PCB manufacturing PCB manufacturing
Home > Blog

Wearable PCB Manufacturing & Assembly for Compact Devices

November 4th, 2026

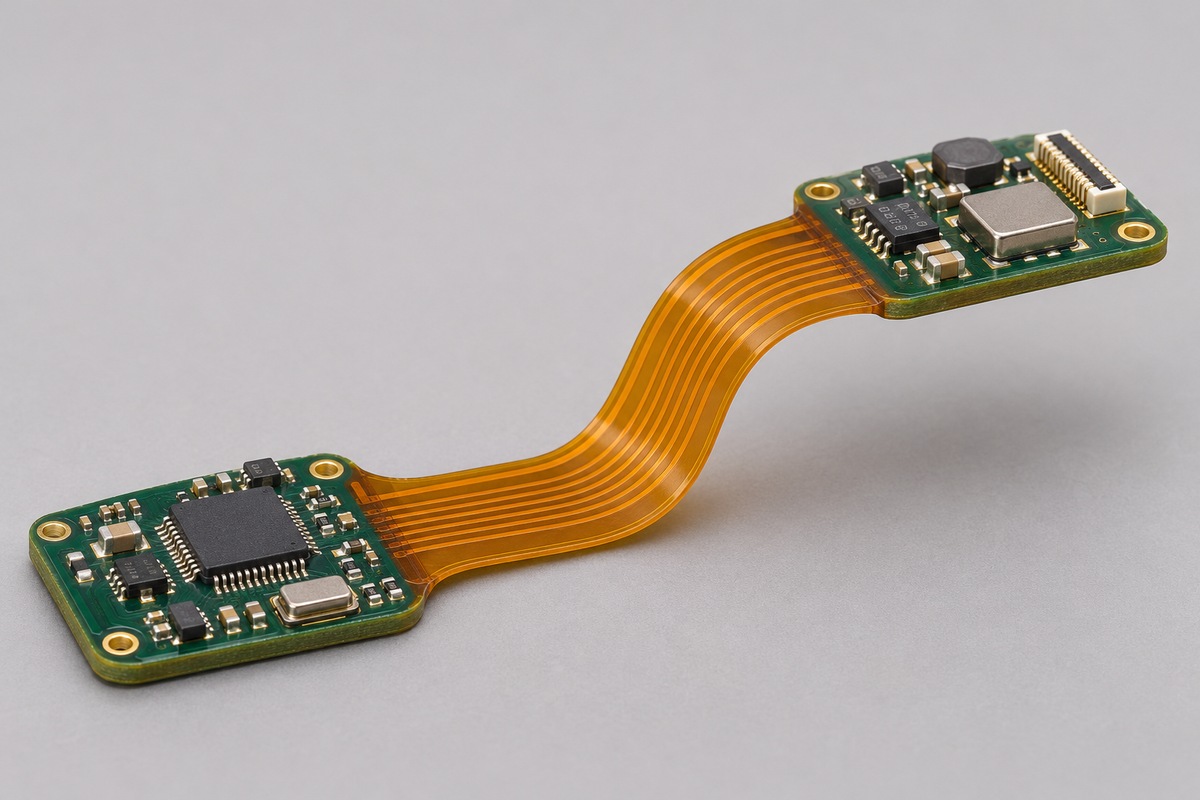
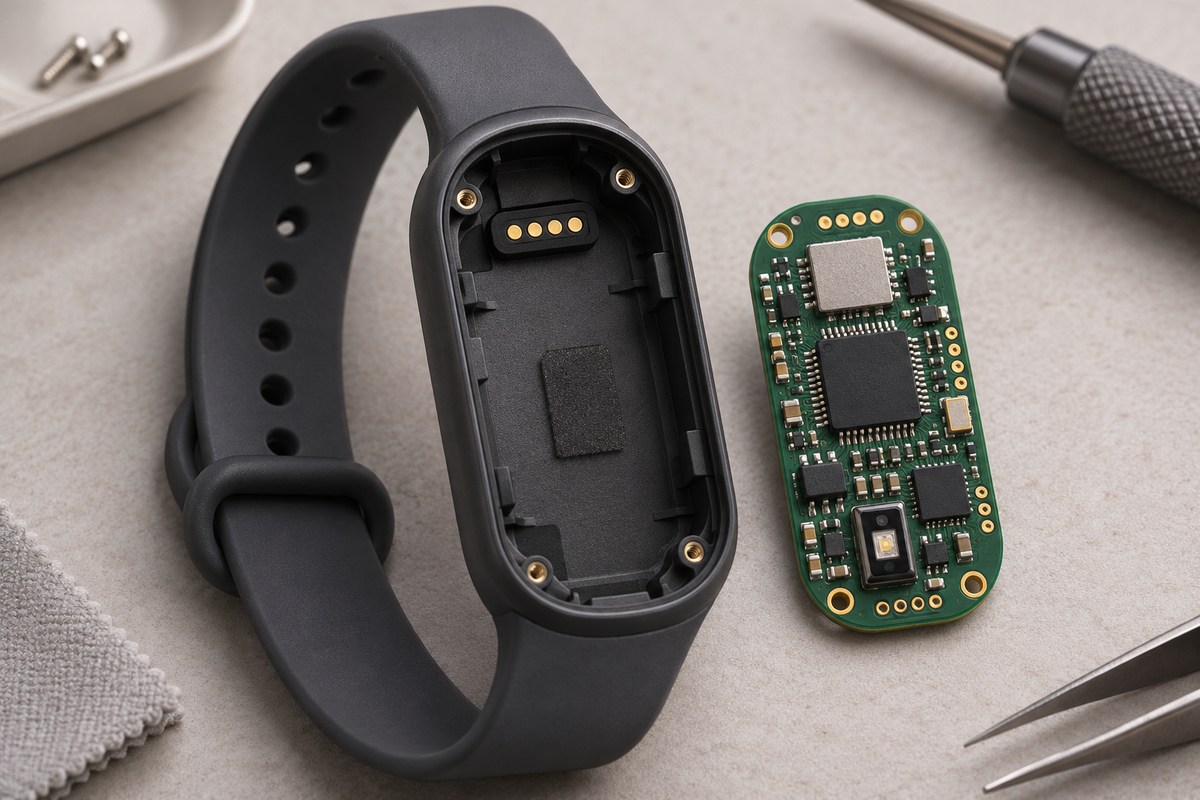
A wearable PCB connects the sensors, power supply and wireless electronics inside a body-worn device. A tracker with a flat, sealed housing may use a small rigid board. A hearing aid with a microphone and receiver at different angles may need a flexible interconnect. The first manufacturing decision is where the components must sit and which parts of the circuit, if any, must bend.

EBest Circuit manufactures and assembles rigid, flex and rigid-flex boards to customer-approved designs. For compact products, our engineering review connects bare-board decisions with assembly requirements, from the panel that carries a small board through reflow to the pads a test fixture must reach. For a review of your wearable PCB design and a project-specific quotation, contact sales@bestpcbs.com.
wearable PCB

Wearable Electronics PCB Manufacturing at EBest Circuit

EBest Circuit supplies bare boards and assembled wearable electronics PCBs. On a tracker small enough to sit under a watch strap, the finished outline determines how the board fits the housing. The panel dimensions determine how it travels through assembly.

Manufacturing Item EBest Circuit Capability
FR-4 layer count, standard 1–10 layers (high-Tg from 8 layers)
FR-4 board with a 5–10 mm side Supplied in panel format
Standard FR-4 thickness, OSP or ENIG 0.4–3.5 mm
Standard FR-4 thickness, HASL 0.6–3.5 mm
Inner traces, 0.5 oz copper 4/4 mil standard, 3/3 mil special
Outer traces, 1 oz copper 4/4 mil standard, 3/3 mil special
Laser blind/buried via diameter 0.10 mm, subject to stackup review
Minimum finished hole diameter 0.20 mm standard, 0.15 mm special
All-flex PCB, one standard route 1–4 layers, 0.06–0.60 mm finished thickness
  • Trace dimensions. The paired values give line width and spacing. Both depend on the copper weight on that layer.
  • Stackup review. Layer count, finished thickness and via span must work in the same construction. Confirm the combination before releasing the layout.
  • Assembly panel. Agree on the panel size separately from the single-board outline so the rails and tooling suit the assembly line.

Flexible PCB for Wearable Electronics: When to Choose Rigid, Flex or Rigid-Flex

Choose a flexible PCB for wearable electronics when the circuit must follow a fold or move during use. If all components fit on one fixed plane, a rigid board may be the simpler build even inside a curved enclosure.

Comparison Item Rigid PCB Flex PCB Rigid-Flex PCB
Typical fit Flat module Folded tail or moving strap Modules on different planes
Component support Rigid laminate Local stiffeners where needed Rigid component sections
Assembly concern Panel separation Carrier support during reflow Fold alignment and transition clearance
Cost drivers Layers and routing density Stiffeners and tooling Combined buildup and panel utilization
wearable PCB
  • One-time fold. A wearable flex PCB tucked behind a display bends during installation. Show the assembled shape, fold direction and available radius.
  • Repeated motion. A flexible PCB for wearable devices that move with a strap needs a defined motion range and cycle requirement. Two circuits with the same flat outline can need different constructions.
  • Connected modules. A wearable rigid-flex PCB can replace a separate connector between modules. Check the folded dimensions and component clearances before comparing its cost with two rigid boards and a cable.

HDI PCB for Wearable Devices: When Do You Need Microvias?

Consider an HDI PCB for wearable devices when conventional vias leave too little room to route signals out of the most crowded component footprint. Start with the package pad array and the layers those signals must reach.

  • Check the escape path. A through via takes up space on every layer it crosses. A blind microvia can connect a surface pad to a nearby layer while leaving deeper layers free for routing.
  • Compare fine lines with another buildup cycle. Finer traces may clear a short routing bottleneck. If several inner rows still have no exit path, review a microvia option against the copper weight and spacing available on the escape layer.
  • Resolve via-in-pad details. Specify the via diameter and layer span. Where the via sits in a solderable pad, agree on filling and capping with the fabricator so the finished pad also suits assembly.

Wearable IoT PCB Requirements for Health Monitors and Trackers

A wearable IoT PCB must fit the sensor, battery and antenna in their operating positions. An assembled view helps the board supplier see constraints that are easy to miss in a flat layout.

  • Sensor alignment. For an optical wrist monitor, check the sensor height against the enclosure window. For a hearing aid, check microphone orientation against the acoustic opening. A PCB manufacturer for wearable health monitors needs both the placement drawing and the mechanical tolerances to review that fit.
  • Antenna clearance. When evaluating a wearable tracking device PCB manufacturer, ask how the antenna keepout and feed geometry will be preserved during fabrication. Nearby metal, the battery and the wearer can affect tuning. Review the 2.4 GHz PCB antenna manufacturing requirements and evaluate radio performance in the intended housing.
  • Battery measurements. Leave fixture access to measure sleep current and radio activity before sealing the tracker. Define the operating state for each reading so the results can be compared across units.

Wearable PCB Design Checks Before Fabrication

A wearable PCB design review should resolve discrepancies between the electrical layout, the enclosure drawing and the assembly panel before tooling starts. Four checks have particular value on compact builds.

  • Outline and height. Compare the finished outline and its tolerance with the housing pocket. Include the mounted height of the tallest component, solder joints and any stiffener or adhesive beneath the board.
  • Connector access. A wearable PCB connector may fit on the layout while leaving no room to insert the flex tail or operate its latch. Check the insertion direction against the battery and housing wall in the assembled view.
  • Bend and transition areas. Mark the bend location on the fabrication drawing. Review nearby vias, solder lands and stiffener edges against that location so the circuit bends where the mechanical design intends.
  • Panel and separation method. Agree on rail positions, fiducials and breakaway tabs. A tab close to a small ceramic component or a sensor can put stress on the assembly during separation. Move the tab or revise the separation method while the panel is still on the drawing.

PCB Assembly for Wearable Electronics

PCB assembly for wearable electronics starts with keeping the board stable through paste printing, placement and reflow. Three decisions deserve attention before the first unit reaches the line.
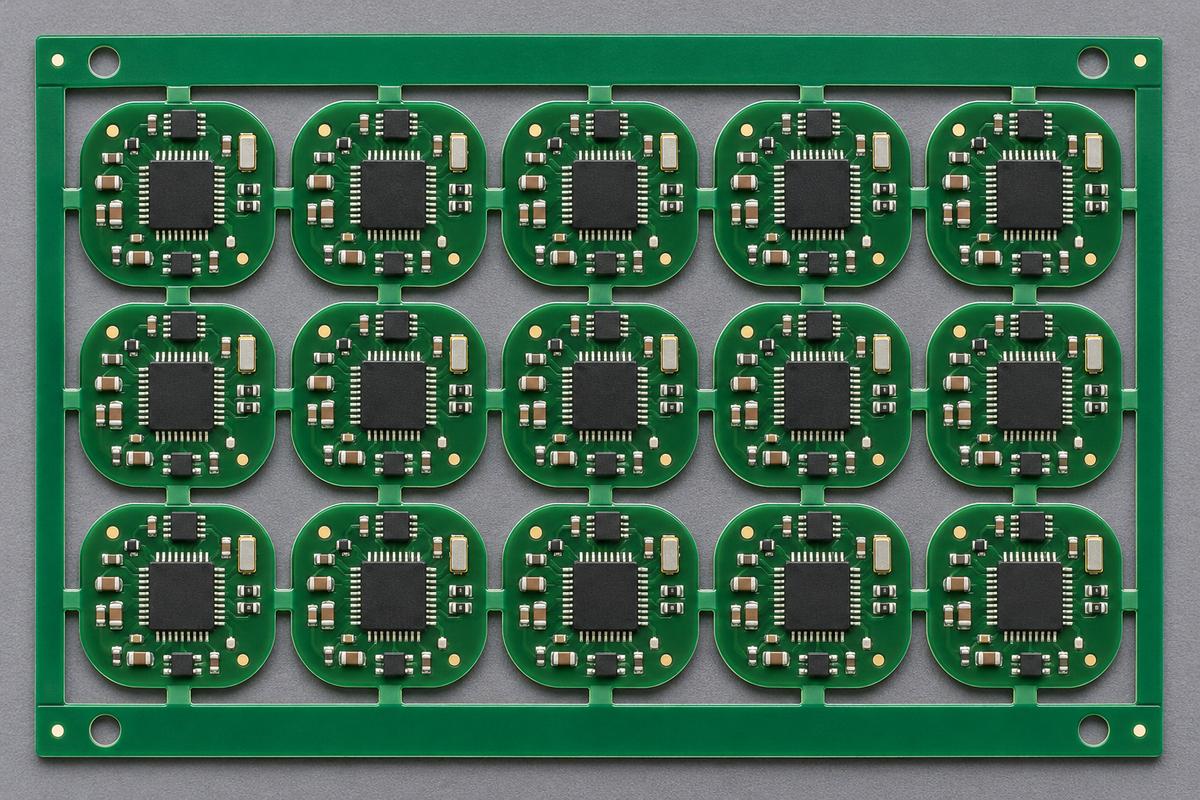
wearable PCB
  • Board support. A small rigid board can stay in its panel through assembly. Flex PCB assembly for wearable devices may require a carrier that supports component areas and leaves clearance for parts already mounted underneath.
  • Placement orientation. Match the assembly drawing, BOM and placement coordinates by reference designator. A sensor rotated by 180 degrees can still fit its footprint. A visible pin-one mark and a drawing at the correct revision help catch that error before reflow.
  • Sensitive components. PCB assembly for wearable health monitors may involve an optical window or a microphone port that needs protection during handling. Check the component supplier’s cleaning instructions when planning the stencil, fixture and cleaning process.

Wearable PCB Assembly Inspection and Functional Testing

For wearable PCB assembly, select each inspection method according to the defect or function it can detect. Agree on coverage and acceptance criteria before the build.

Inspection Method Inspection Focus Applicable Stage
Bare-board electrical test Netlist opens and shorts Before assembly
Solder paste inspection Deposit position and volume After printing
Automated optical inspection Visible placement and solder defects After reflow
X-ray inspection Hidden joints, including BGA joints After reflow, as specified
Functional test Startup, sensor response or sleep current Assembled board with test firmware
  • Fixture access. Place circuit board test points where the fixture can reach the required rails and signals.
  • Acceptance records. For a high-reliability wearable PCB project, define the firmware revision, test sequence, limits and results to record per unit or lot.
  • Device validation. A board-level test can confirm that a sensor responds. Measurement accuracy on the body requires separate validation of the finished device.

What Drives the Cost and Lead Time of a PCB for Wearables?

For a PCB for wearables, the lowest bare-board unit price does not always give the lowest assembled cost. A rigid-flex design can cost more to fabricate yet remove a connector and a manual connection step. Compare both options at the same production quantity and test coverage.

  • Fabrication cost depends on how many boards fit on a manufacturing panel, the layer buildup, the via process and any special tolerances. An irregular outline can use more panel area than its finished dimensions suggest.
  • One-time costs can include a stencil, flex carrier, programming fixture or functional test fixture. Separate these charges from the recurring unit price, particularly when comparing a prototype lot with a repeat order.
  • Lead time depends on the latest available input. A finished PCB cannot enter assembly until the approved sensor, connector and other required parts are available. Ask for fabrication, procurement, assembly and test milestones when a prototype date matters.

Why Choose EBest Circuit as Your Wearable Device PCB Manufacturer?

EBest Circuit can review the bare board and assembly as a single build. For a compact product, that lets the buyer resolve issues that cross supplier boundaries while the drawings can still change.

  • Panel planning: Small-board delivery requirements can be reviewed alongside assembly rails and depaneling locations, so the quoted panel suits both fabrication and placement.
  • Process selection: Distinguishing standard trace spacing from special processing gives the layout team a concrete choice between revising a local bottleneck and paying for tighter geometry.
  • Construction review: Rigid, flex and rigid-flex options can be assessed against the same mechanical drawing. The comparison accounts for component support, connectors and assembly steps as well as board price.
  • Assembly preparation: Reviewing the BOM, coordinates and assembly drawing together helps resolve orientation, package and material questions before the first build.
  • Inspection planning: Visible joints, hidden joints and functional checks can be assigned appropriate inspection methods. The customer can define the required coverage and records before accepting a quotation.

How to Request a Wearable PCB Quote

Send EBest Circuit a fabrication package for a bare-board quote. For an assembled board, add the placement and test information so the quotation covers the product you intend to receive.

  • PCB files: Gerber and drill data or ODB++, a dimensioned outline, stackup, finished thickness, copper weights, surface finish and impedance requirements where applicable.
  • Mechanical details: An enclosure or folded view, component height limits, bend zones, stiffeners and critical tolerances.
  • Assembly files: A BOM with manufacturer part numbers and approved alternatives, placement coordinates, an assembly drawing and any consigned-part details.
  • Commercial and test scope: Prototype and repeat-order quantities, requested delivery date, programming requirements, test limits and the inspection records needed at delivery.

If the board construction is still open, identify the dimension or assembly step that is driving the decision. That gives the engineer a specific constraint against which to compare options.

FAQs About Wearable PCBs

Can I supply sensors or other critical components for assembly?
For a consigned build, include the manufacturer part numbers, available quantities, packaging and handling instructions. Agree on placement allowance and how unused parts will be returned.

Can the same panel be used for prototypes and production?
Often it can, provided the panel remains compatible with assembly equipment, test access and the separation method. Confirm before ordering repeat boards if the quantity or assembly route changes.

Should a sensor with the same footprint be accepted as a substitute?
Footprint compatibility is only one check. Review pin functions, firmware support, operating range and any calibration requirements, then obtain approval before substitution.

What should happen if the firmware changes after the pilot build?
Identify the firmware revision by lot or serial number and define which previously built units need reprogramming or retesting. Include the revision in the test record.

Can coating be applied around microphones, contacts or optical sensors?
Define keepout areas on the coating drawing and check the component supplier’s restrictions. An acoustic port, mating contact or optical window may need masking even when nearby circuitry is coated.

How should a bend-life requirement be specified?
Give the bend radius, angle, direction, number of cycles and electrical failure criterion. These conditions allow the fabricator and customer to agree on a representative test structure.

EBest Circuit handles both board fabrication and component assembly for wearable PCB projects. Reviewing the two together helps us spot details that affect the finished device, such as a connector that fits on the bare board but leaves too little room to operate its latch once the battery is installed. To discuss the board construction and assembly options for your next build, send your layout and enclosure drawing to sales@bestpcbs.com.
You may also like

Solder Wetting in PCB Assembly: Causes, Defects and Solutions

November 4th, 2026

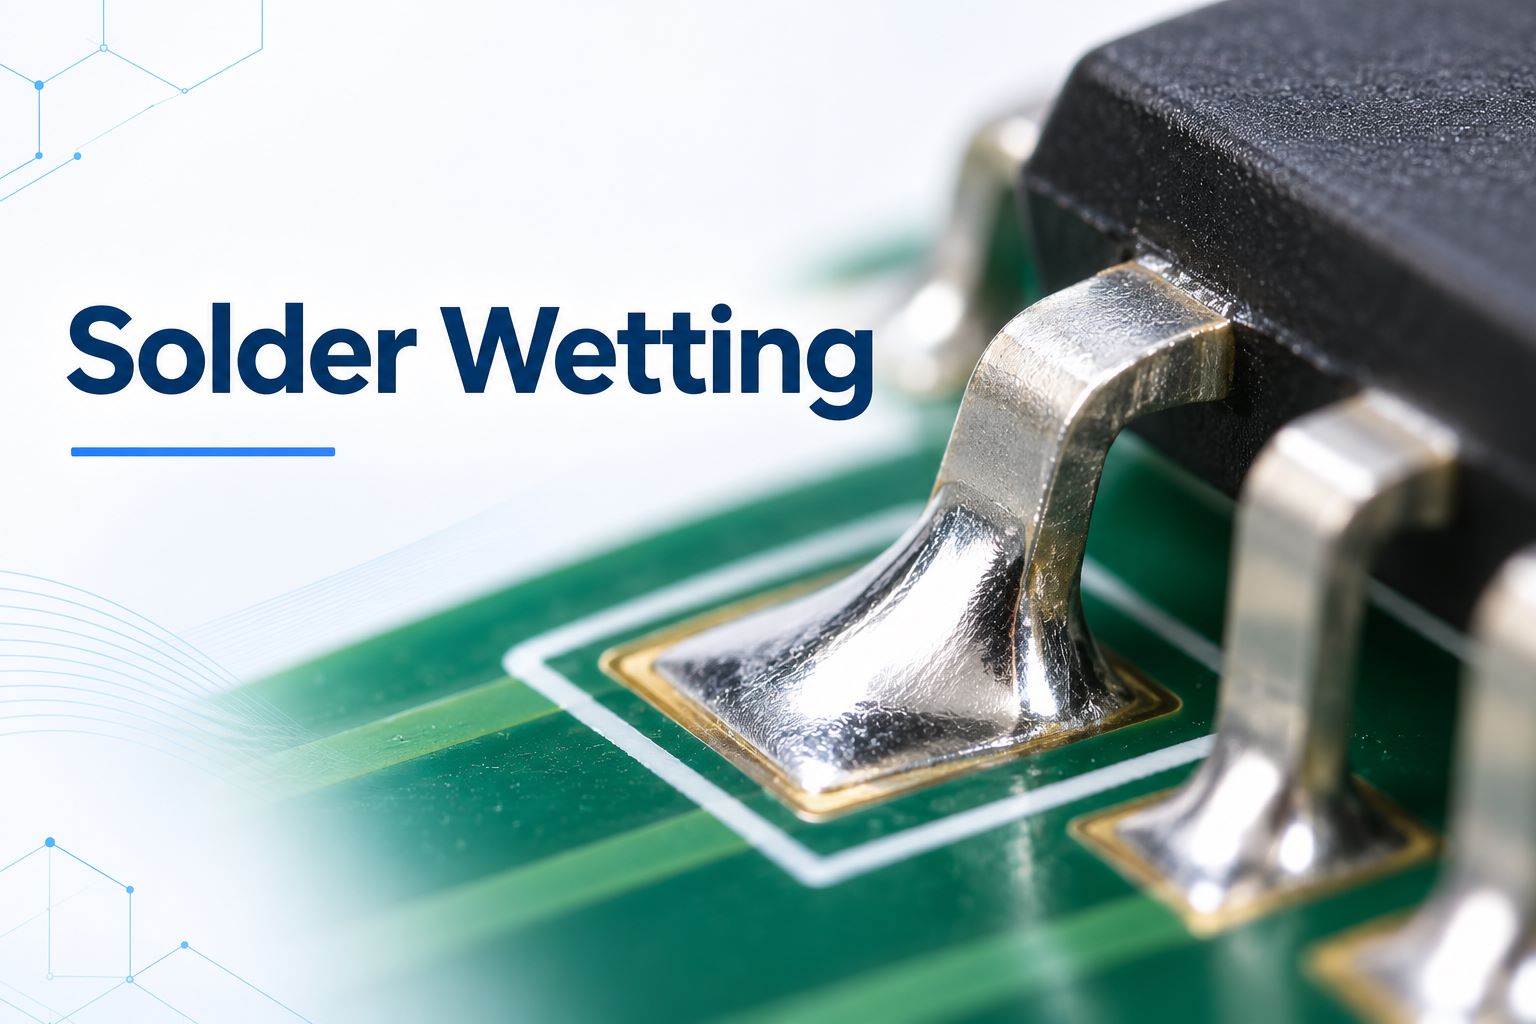
Solder wetting plays a critical role in PCB assembly by ensuring molten solder forms strong electrical and mechanical connections between PCB pads and component terminals. Poor wetting can lead to weak joints, incomplete solder coverage, and unreliable connections. This guide explains how solder wetting works, what causes common defects, and how to test, prevent, and resolve wetting problems.

At EBest Circuit (Best Technology), we support consistent solder wetting through free DFM reviews, controlled solder paste printing, nitrogen reflow, and SPI/AOI inspection. With four SMT production lines, 01005 component capability, and MES traceability, we provide reliable PCB assembly services from prototypes to mass production. Send your Gerber files, BOM, and quantity to sales@bestpcbs.com for a free DFM review and PCBA quotation.

solder wetting

What Is Solder Wetting and Why Does It Matter?

Solder wetting describes how molten solder spreads over and adheres to a solderable metal surface. During PCB assembly, solder wets the PCB pad and component termination, forming intermetallic compounds (IMCs) at the interface that contribute to a metallurgical bond.

Good wetting supports:

  • Electrical conductivity: Creates a continuous connection between components and PCB pads.
  • Mechanical strength: Supports the structural integrity of solder joints.
  • Joint consistency: Promotes suitable solder coverage and fillet formation.
  • Product reliability: Reduces the risk of wetting-related connection failures.

For example, a chip resistor may appear correctly positioned after reflow, but incomplete wetting at one termination can compromise its electrical connection.

The quality of wetting depends mainly on surface condition, solder alloy, flux activity, and soldering temperature. These factors should be considered together during material selection and assembly process development.

How Does the Solder Wetting Process Work?

The solder wetting process involves cleaning the metal interface, melting the solder, spreading across the surface, and forming a metallurgical bond. During SMT reflow, these reactions occur as the assembly passes through a controlled temperature profile.

The process follows five main stages:

  1. Surface Preparation: PCB pads and component terminations provide suitable solderable surfaces. Surface finishes such as ENIG, OSP, immersion silver, and immersion tin help protect the underlying metal before assembly.
  2. Flux Activation: Flux removes or disrupts oxides and helps protect the metal surfaces during heating.
  3. Solder Melting: The solder alloy reaches its melting range. SAC305 lead-free solder melts around 217–220°C, while Sn63Pb37 melts at approximately 183°C.
  4. Wetting and Bonding: Molten solder spreads across the metal surfaces, forming intermetallic compounds at the interface.
  5. Cooling: The solder solidifies and forms the final joint.

For tin-based solder on copper, Cu₆Sn₅ is a common intermetallic compound. Controlled intermetallic formation supports bonding, while excessive growth can affect joint properties.

The final joint shape depends on pad geometry, component termination, solder volume, and thermal conditions.

What Is a Good Solder Wetting Angle?

The solder wetting angle, or contact angle, measures the angle between molten solder and the solid metal surface at their contact point. A smaller angle generally indicates better solder spreading.

Wetting AngleGeneral Interpretation
0°Idealized complete wetting
Below 90°Wetting
90°Boundary condition
Above 90°Non-wetting

These values describe general wetting behavior rather than universal PCB solder joint acceptance limits.

In actual PCB assembly, engineers also evaluate solder fillets, joint coverage, and component-specific acceptance requirements.

A properly wetted solder joint generally shows:

  • Continuous solder coverage on the intended surfaces.
  • Suitable solder fillet formation.
  • Smooth transitions between solder and metal surfaces.
  • No obvious exposed areas caused by incomplete wetting.

The expected appearance varies between chip resistors, gull-wing leads, and BGA packages. Therefore, joint acceptance should follow the applicable IPC standards and component requirements rather than a single contact angle value.

Non-Wetting vs. Dewetting Solder: What’s the Difference?

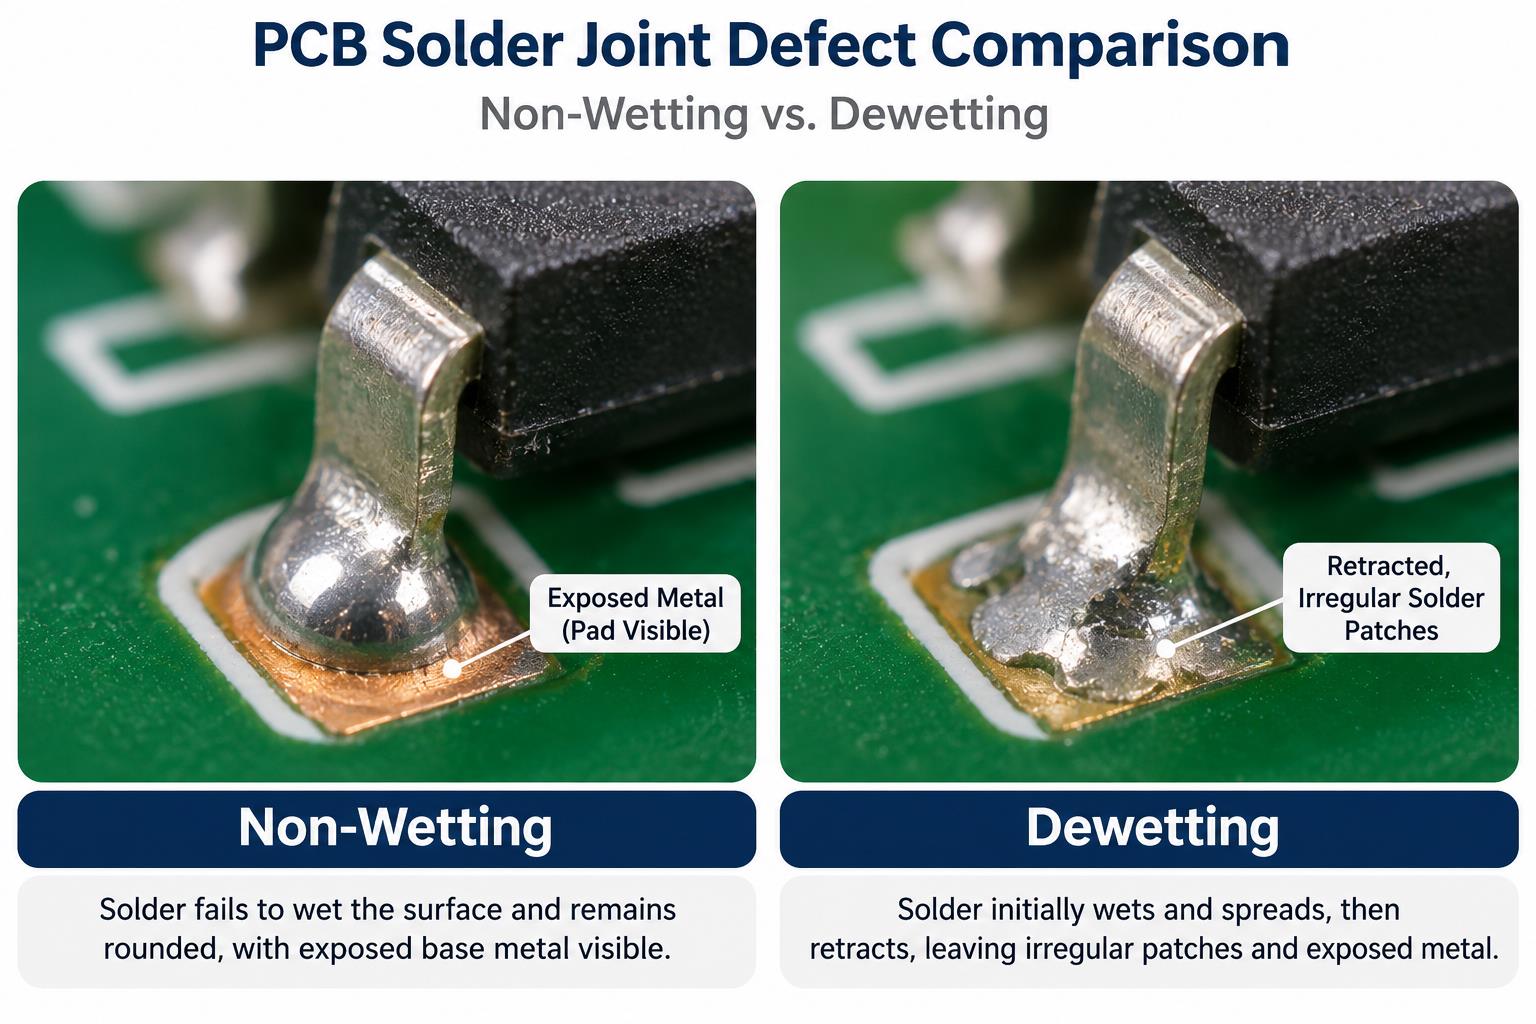
Non-wetting and dewetting are different soldering defects. Non-wetting occurs when molten solder fails to form an adherent coating on a metal surface. Dewetting occurs when solder initially wets the surface but later retracts, leaving exposed areas.

solder wetting
ComparisonNon-WettingDewetting
Initial behaviorSolder fails to wetSolder initially wets
AppearanceExposed metal, rounded solderIrregular solder patches
Surface coverageIncomplete from the startDecreases after spreading
Common concernsOxidation, contamination, poor solderabilityOxidation, metallization, thermal exposure

Non-Wetting: Molten solder may remain rounded instead of spreading across a PCB pad or component lead. Oxidized surfaces, unsuitable flux, and poor component solderability are common contributing factors.

Dewetting: Solder initially spreads but subsequently pulls away from portions of the surface. This can result from changes in surface condition, metallization problems, or unsuitable thermal exposure.

The distinction matters during troubleshooting. For non-wetting, engineers should first examine surface cleanliness and solderability. For dewetting, they should also investigate metallization quality and the soldering thermal profile.

What Causes Poor Solder Wetting in PCB Assembly?

Poor solder wetting usually results from oxidation, contamination, unsuitable solder materials, or incorrect thermal conditions. Identifying the actual cause is essential because increasing reflow temperature alone may not resolve the defect.

The following table summarizes common causes and their effects.

CauseEffect on Solder Wetting
PCB pad oxidationPrevents proper solder spreading
Component terminal oxidationReduces termination solderability
Insufficient flux activityLeaves surface oxides
Incorrect reflow profileDisrupts melting and wetting
Unsuitable solder pasteAffects soldering performance
Surface contaminationRestricts metal-to-solder contact
Poor metallizationCreates an unsuitable solder interface

PCB and Component Oxidation: Oxide layers interfere with the contact between molten solder and the metal surface. Proper packaging, controlled storage, and incoming inspection help maintain solderability.

Flux and Solder Paste Problems: Flux must provide sufficient activity for the selected surface finishes. Expired or improperly handled paste can affect printing and soldering performance.

Reflow Temperature: Insufficient heating may limit solder spreading, while excessive exposure can accelerate oxidation and intermetallic growth.

Surface Finish Problems: Coating defects, unsuitable metallization, and degraded surface finishes can also affect wetting.

When defects occur only on specific components or PCB batches, comparing the affected material with a known-good lot can help identify the source.

How Do Reflow Temperature and Solder Paste Affect Wetting?

Reflow temperature determines when solder melts and how long it remains liquid, while solder paste supplies the alloy and flux required for wetting. Both must work together to achieve consistent solder joint formation.

Reflow Temperature Control

Reflow StageFunction
PreheatGradually heats the PCB
SoakSupports flux activity and thermal uniformity
ReflowMelts solder and enables wetting
CoolingSolidifies the solder joint

Two important parameters are peak temperature and time above liquidus (TAL). Both should follow the solder paste manufacturer’s process recommendations and the thermal limits of the PCB and components.

For SAC305 solder, the melting range is approximately 217–220°C. The required peak temperature is higher than the melting range and depends on the approved process window.

Solder Paste Selection

The following factors influence soldering performance:

  • Alloy composition: Determines melting characteristics.
  • Flux activity: Supports oxide removal and solder spreading.
  • Paste condition: Affects printing and process stability.
  • Solder volume: Influences final joint geometry.

Nitrogen reflow can further support wetting by reducing oxidation during soldering. It is particularly useful for oxidation-sensitive assemblies and certain fine-pitch applications.

However, consistent results still depend on clean surfaces, compatible solder paste, and a properly developed reflow profile.

How to Prevent and Fix Solder Wetting Defects?

Preventing solder wetting defects requires suitable materials, controlled solder paste printing, and a validated reflow process. When a defect appears, engineers should identify its cause before applying corrective action.

Practical Troubleshooting Guide

DefectCheck FirstCorrective Action
Solder does not spreadPCB pad oxidationReview surface finish
Solder beads on padFlux and surface conditionVerify flux compatibility
Solder retractsMetallization and heatingInvestigate dewetting
Poor wetting on leadsComponent solderabilityCheck component lot
Uneven wettingReflow temperatureMeasure thermal profile
Inconsistent joint formationPaste printingReview SPI results

A reliable troubleshooting process follows five steps:

  1. Identify the defect: Examine solder coverage, joint shape, and affected component locations.
  2. Check the materials: Review PCB finishes, component terminals, solder paste, and storage conditions.
  3. Verify printing: Use SPI results to identify paste volume or alignment problems.
  4. Measure reflow conditions: Check peak temperature, time above liquidus, and temperature uniformity.
  5. Confirm corrective action: Reinspect the solder joints and compare results with the original defect.

For recurring issues, production records should include PCB lot numbers, component batches, solder paste details, and reflow profile information.

Rework considerations: Some wetting defects can be corrected through controlled rework. The joint condition, component temperature limits, and applicable acceptance criteria should determine whether rework or replacement is appropriate.

How Are Solder Wetting and Solderability Tested?

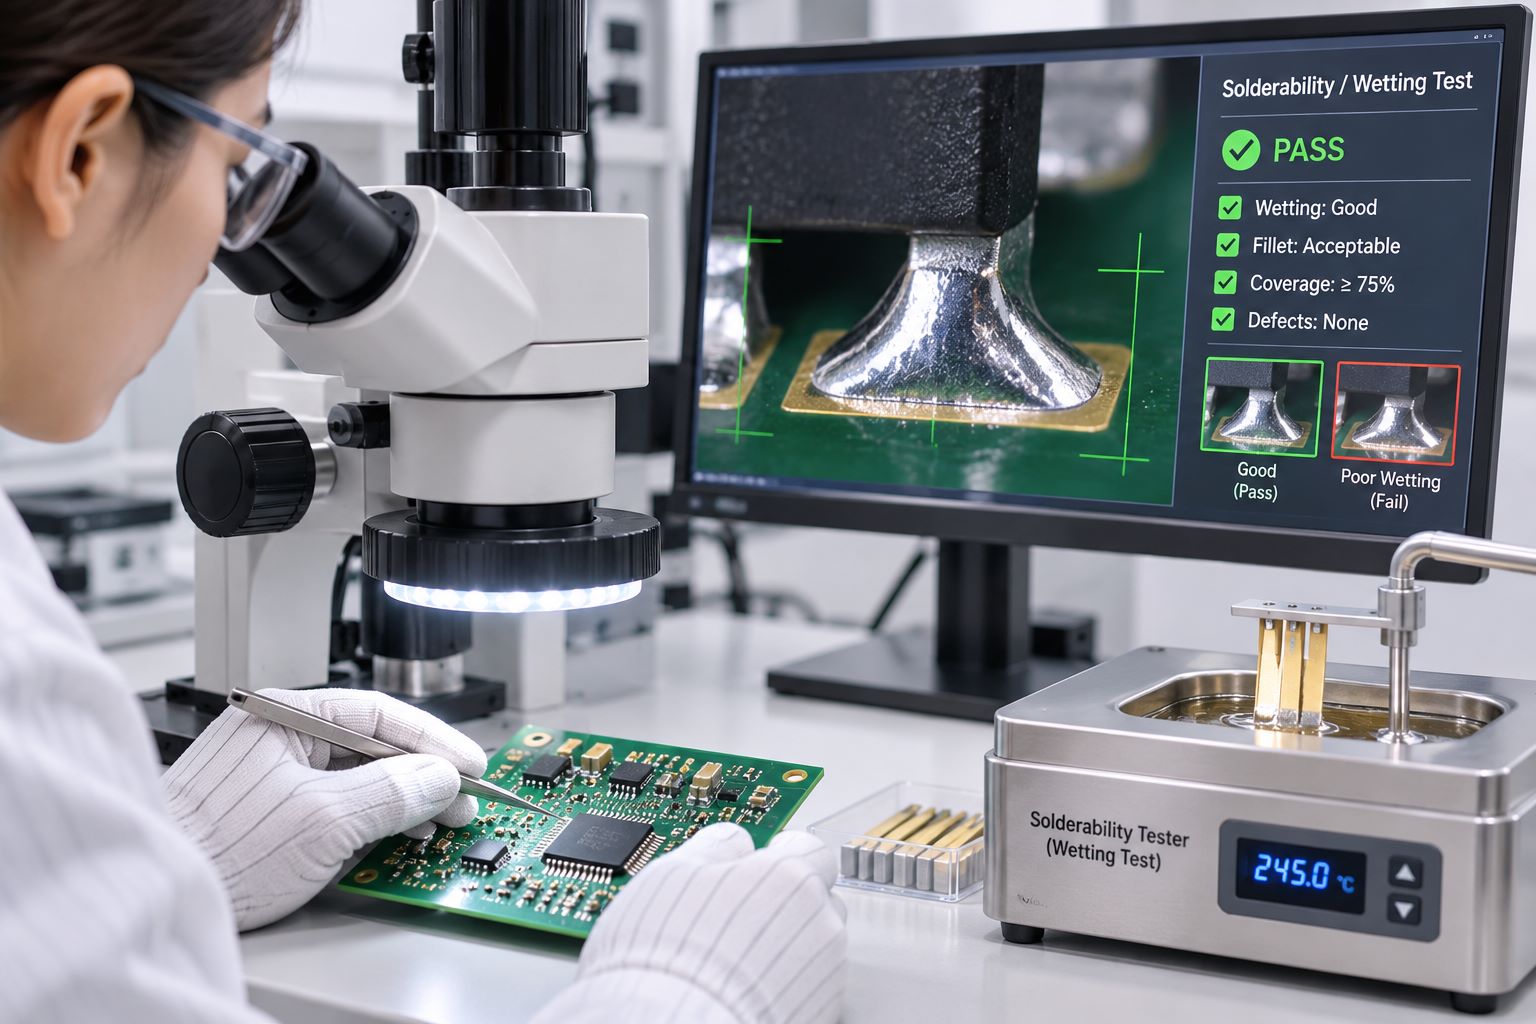
Solder wetting tests evaluate how molten solder spreads or interacts with a metal surface. Solderability tests determine whether PCB finishes and component terminations can form suitable solder connections under defined conditions.

solder wetting

Different methods are used for incoming materials, assembled PCBs, and failure analysis.

Test MethodMain Purpose
Wetting balanceMeasures wetting force over time
Dip-and-lookEvaluates solder coverage
Contact angle testMeasures solder spreading
Visual inspectionIdentifies visible wetting defects
AOIDetects visible joint abnormalities
X-RayExamines hidden joint geometry
Cross-sectionEvaluates internal solder interfaces

Wetting Balance Test: Measures force changes as a specimen contacts molten solder. The resulting curve provides information about wetting behavior.

Dip-and-Look Test: Evaluates solder coverage after a component termination or other specimen is exposed to molten solder under controlled conditions.

AOI and X-Ray: AOI identifies visible assembly defects, while X-Ray examines hidden solder joint structures, including BGA connections. Neither method alone proves complete metallurgical wetting.

Relevant IPC Standards

  • IPC-A-610: Electronic assembly acceptability.
  • J-STD-001: Requirements for soldered electronic assemblies.
  • J-STD-002: Component solderability testing.
  • J-STD-003: Printed board solderability testing.

Solderability testing is particularly useful when materials have been stored for extended periods, a new supplier is introduced, or repeated wetting defects appear in a specific production batch.

How EBest Circuit Controls Solder Wetting Quality in PCBA

At EBest Circuit (Best Technology), solder wetting quality is supported by coordinated DFM review, solder paste inspection, nitrogen reflow, AOI, X-Ray, and MES production traceability.

With 20 years of electronics manufacturing experience, we combine PCB fabrication, component sourcing, PCB SMT assembly, inspection, and testing to support customers from prototypes to repeat production.

Our SMT Manufacturing Capabilities

CapabilityEBest Circuit
SMT production lines4: JUKI × 2, YAMAHA × 2
Smallest SMT component01005
BGA capability0.2 mm pitch
Reflow equipmentNitrogen reflow
Solder paste inspection3D SPI
Joint inspectionAOI and X-Ray/AXI
Electrical testingICT and FCT
TraceabilityMES, approximately 5-second retrieval
Minimum order quantityNo MOQ

How We Control Soldering Quality

  • Free DFM Review: Our engineers review pad geometry, component footprints, stencil considerations, and assembly risks before manufacturing.
  • 3D SPI Inspection: Monitors solder paste deposits to identify printing abnormalities before reflow.
  • Nitrogen Reflow: Helps reduce oxidation and supports consistent soldering conditions.
  • AOI and X-Ray Inspection: Evaluate visible and hidden solder joint abnormalities using the appropriate inspection method.
  • MES Traceability: Supports production record tracking and defect investigation at the individual PCB level.
  • Engineering Support: One sales representative and three engineers coordinate technical questions, production requirements, and quality feedback.

Our quality management systems include ISO 9001, ISO 13485, IATF 16949, and AS9100D, supporting customer supplier qualification and controlled manufacturing requirements.

Need reliable PCB assembly with controlled soldering processes? EBest Circuit offers no-MOQ production, four SMT lines, nitrogen reflow, engineering support, and traceable quality control. Send your Gerber files, BOM, quantity, and target delivery date to sales@bestpcbs.com for a free DFM review, quotation, and production schedule confirmation.

FAQs About Solder Wetting

1. What Is the Difference Between Solder Wetting and Solderability?

Solder wetting describes how molten solder spreads across a metal surface. Solderability describes a material’s ability to form a suitable solder connection under specified conditions. Good solderability supports successful wetting during assembly.

2. What Is Insufficient Wetting in Soldering?

Insufficient wetting occurs when solder fails to spread adequately over the intended metal surface. Typical signs include exposed pads, incomplete solder coverage, and irregular solder fillets.

3. Does Lead-Free Solder Have Poorer Wetting Than Leaded Solder?

Some lead-free alloys have different wetting characteristics and higher melting temperatures than traditional tin-lead solder. Suitable flux, clean surfaces, and a controlled reflow profile help achieve reliable lead-free joints.

4. Can Poor Solder Wetting Cause PCB Failure?

Yes. Poor wetting can weaken electrical and mechanical connections, potentially causing intermittent faults or joint failures, particularly under thermal cycling or vibration.

5. Can Poor Solder Wetting Be Repaired?

Some defects can be corrected through controlled rework. Engineers should first identify the cause and evaluate pad and component condition. Damaged or severely oxidized surfaces may require replacement.

6. What Is the Best Way to Prevent Solder Wetting Problems?

Use solderable PCB finishes and components, compatible solder paste, controlled storage, verified stencil printing, and a suitable reflow profile. SPI, AOI, and traceability records help maintain consistent production quality.

Reliable solder joints start with the right materials, well-controlled soldering conditions, and effective inspection. EBest Circuit (Best Technology) combines 20 years of electronics manufacturing experience, four SMT lines, nitrogen reflow, SPI/AOI/X-Ray inspection, and MES traceability to help customers maintain consistent soldering quality. Backed by ISO 9001, ISO 13485, IATF 16949, and AS9100D certifications, we offer no-MOQ PCB assembly with engineering support from prototype validation to repeat production. Share your PCB design files, BOM, quantity, and delivery requirements with sales@bestpcbs.com for a manufacturing review, quotation, and lead-time confirmation.

You may also like

Precision 0201 PCB Assembly Services for Prototypes and Production

November 3rd, 2026

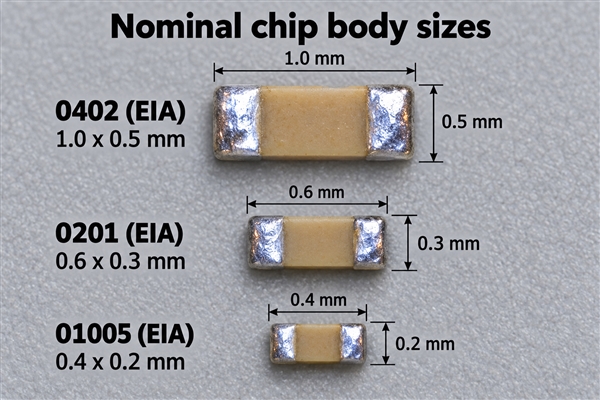
0201 PCB assembly helps manufacturers fit more functionality into compact electronic products while keeping small-component placement and soldering under control. For a board populated with miniature resistors and capacitors, a successful build depends on matching the component, footprint, printed solder paste and reflow process. Here, 0201 refers to the imperial package designation, commonly associated with a nominal body size of 0.6 × 0.3 mm and the metric code 0603.

At EBest Circuit (Best Technology), we offer PCB fabrication, component sourcing and assembly support for prototype and production projects. Our SMT capabilities extend down to 01005 components and include solder paste inspection, placement, reflow and automated optical inspection. Email sales@bestpcbs.com to discuss your 0201 assembly requirements, order quantities and testing scope.

0201 PCB assembly

What Does Our 0201 PCB Assembly Service Include?

Our 0201 PCB assembly service combines board manufacturing, component supply, SMT assembly and project-specific testing. You can source the complete assembly through EBest Circuit or use a supply arrangement that incorporates materials you already own.

  • Full turnkey assembly. We manufacture the PCB, procure the components and assemble the board. This suits projects where your team wants one supplier to coordinate the bare boards and the populated assemblies.
  • Partial turnkey assembly. You supply selected components, and we source the remaining items. This is useful when a processor, custom device or long-lead component has already been purchased.
  • Consignment assembly. You provide the boards and components for assembly. Material quantities, packaging and readiness are reviewed before scheduling the build.

For 0201 orders, the service connects three areas that directly affect the finished board.

  • Component and footprint compatibility. DFA and incoming inspection help establish whether the supplied parts match the BOM and intended mounting geometry. The exact manufacturer part number identifies the body, termination and electrical specifications.
  • Printing and placement. Stencil fabrication, solder paste printing, placement and reflow turn the approved design into soldered connections. Small 0201 deposits require consistent printing and suitable termination overlap.
  • Inspection and testing. The inspection scope addresses assembly workmanship, while agreed functional tests assess the required circuit behavior. Test development and fixture needs can be included in the project discussion.

The quotation can therefore cover the complete assembled-board requirement, including the chosen sourcing arrangement and testing scope.

What Capabilities Support Reliable 0201 Component Assembly?

Reliable 0201 assembly requires repeatable solder deposits, accurate component placement and a thermal process suited to the complete board. Small changes become significant when each component body is only a fraction of a millimeter wide.

Our equipment includes a Yamaha YSM20R surface mounter, a SINIC-TEK S8080 3D SPI system and a SINIC-TEK A510DL 3D AOI system. These support placement, printed-paste measurement and post-reflow inspection at different stages of the build.

The following comparison shows where imperial 0201 sits among common miniature passive packages.

Imperial package Common metric code Nominal body length × width Calculated body area Assembly consideration
0402 1005 1.0 × 0.5 mm 0.50 mm² Larger features generally provide more room for placement, inspection and rework
0201 0603 0.6 × 0.3 mm 0.18 mm² Smaller deposits and terminations make print and placement consistency more demanding
01005 0402 0.4 × 0.2 mm 0.08 mm² Finer features require further attention to paste release, handling and inspection resolution

An 0201 body occupies 64% less nominal area than a 0402 body. The total board-space saving depends on the pads, component spacing, routing and access requirements.

These dimensions describe component bodies. Footprints, stencil openings, height limits and electrical ratings follow the selected part. In particular, metric 0201M identifies a different, smaller package family, so the sizing convention must remain clear throughout the BOM and assembly data.

Can We Assemble 0201 Components Alongside BGAs and Larger Parts?

Yes. We support boards that combine 0201 passives with BGAs, larger surface-mount devices and through-hole components. The assembly approach depends on how these packages share solder paste, board space and thermal exposure.

Mixed-package assembly has three main process considerations.

  1. Different joints need different solder volumes. An 0201 termination uses a much smaller deposit than a large connector pad. A thick stencil can make paste release difficult through a small opening, while a thin stencil can leave larger joints short of solder. Aperture design and paste selection help balance these requirements. A stepped stencil may be considered where the layout allows separate thickness regions.

  2. Small and large components heat differently. BGAs, connectors and copper-heavy regions can respond differently to reflow than nearby 0201 parts. Profiling evaluates the temperature behavior across representative locations so joint formation and component temperature limits can be assessed together.

  3. The package combination determines inspection access. Optical inspection can examine visible 0201 placement and joints, while BGA connections beneath the package may require X-ray inspection. Close spacing and tall neighboring parts also affect visibility and access for potential rework.

For a compact board with a BGA processor surrounded by 0201 decoupling capacitors, the assembly review needs to consider both package types together. Their paste requirements, thermal behavior and inspection access all contribute to the same build.

Our SMT and mixed-assembly services allow these requirements to be discussed within one PCB assembly project, including any through-hole operations needed for connectors or other larger parts.

0201 PCB assembly

How Do We Support 0201 PCB Assembly from Prototype to Production?

We support initial prototype builds and subsequent production orders, with the assembly scope matched to the stage of the project. For 0201 designs, the transition centers on establishing a workable first build and carrying its relevant manufacturing conditions into repeat orders.

  1. Prepare the first build around the actual parts. The BOM, PCB layout and component packaging establish the starting point for assembly review. Particular attention goes to 0201 footprint compatibility and the supply format available for a small prototype quantity.

  2. Use the prototype to evaluate assembly behavior. Printing, placement, reflow and inspection reveal how the design performs in manufacture. Uneven deposits, component skew or lifted terminations provide specific feedback for a process or layout adjustment. Electrical testing then evaluates the agreed circuit functions.

  3. Resolve changes before increasing quantities. A footprint correction, component substitution or revised test requirement can affect the next build. Incorporating those changes into the approved design and BOM gives the production order a clear manufacturing basis.

  4. Plan repeat orders around material supply and setup. Component availability, tape format, board revision and test requirements affect both scheduling and repeatability. A change from prototype cut tape to production reels, for example, changes the supply and feeder preparation even when the fitted part number remains the same.

Prototype and production quantities can be quoted together. This helps your team compare initial setup costs with later batch pricing and discuss component purchases against expected demand.

Include the first-build quantity and anticipated repeat-order quantities when contacting us. We can review the supply and assembly scope for both stages.

How Do We Control Quality in 0201 PCB Assembly?

Quality control begins with the relationship between the PCB footprint and the selected component, then follows the assembly through printing, placement and soldering. Our process includes DFA checks, incoming inspection, SPI and post-reflow inspection.

For 0201 components, several defects deserve particular attention.

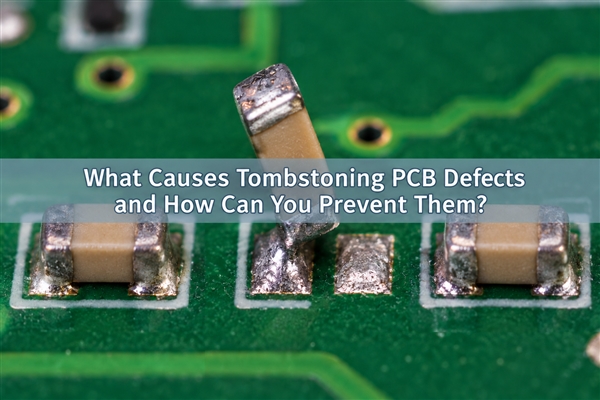
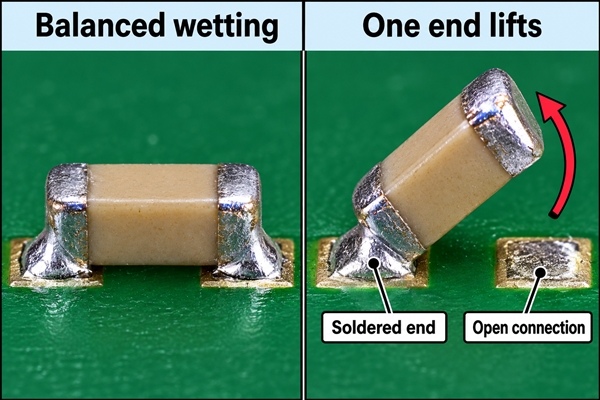
  • Tombstoning. One termination lifts when soldering forces become unbalanced. Land geometry, solder quantity, placement and temperature differences can contribute.
  • Component skew. A rotated or displaced part can reduce termination overlap. Placement condition and the final soldered position both matter.
  • Insufficient solder or open joints. A missing or inadequate deposit can leave a termination poorly connected. Paste inspection helps identify printing problems before reflow.
  • Solder bridging. Excess or misplaced solder can connect conductors that should remain separate. Printing condition, spacing and the finished joint all need evaluation.

SPI provides information about deposited paste, while AOI examines visible features after soldering. On boards containing BGAs or other hidden joints, X-ray inspection addresses features that optical inspection cannot directly view. Functional testing evaluates the specified circuit behavior.

The inspection plan should connect each method to the relevant defect and acceptance requirement. A passing visual inspection alone cannot establish every component value or every aspect of circuit operation.

0201 PCB assembly

What Affects 0201 PCB Assembly Cost and Lead Time?

0201 PCB assembly pricing depends on the complete build. The package size contributes to process demands, while component supply, board complexity, quantities and testing determine much of the total quotation.

Quotation factor Effect on cost Effect on lead time
Component availability and packaging Procurement cost, reel quantities and handling requirements affect the material total A critical unavailable part can delay the complete build
Number of placements and unique parts Placement workload and feeder setup influence assembly effort More setup and verification work can extend preparation
Mixed package sizes and assembly sides Stencil planning, additional passes and process development add work Printing and thermal evaluation may be needed before release
Order quantity and repeat demand Setup costs are distributed across the batch Material planning and production scheduling depend on the required quantities
Inspection and functional testing Programming, fixtures and test time contribute to the quoted scope Fixture preparation or test development can precede assembly completion

A low component count does not automatically produce a low-cost order. A small prototype batch still requires preparation, and a single difficult-to-source device can dominate the schedule.

Similarly, assembly-line processing time is only one part of delivery. PCB fabrication, material readiness, engineering review and testing all affect the date on which finished assemblies can ship.

For a useful quotation, send the Gerber files, BOM with manufacturer part numbers, placement data, assembly drawing, quantities and target delivery date. Include any functional test specification or special acceptance requirement so the price covers the intended finished product.

Why Choose EBest Circuit for 0201 PCB Assembly?

EBest Circuit combines PCB fabrication, component sourcing and assembly support for compact electronic designs. For an 0201 project, that combination helps connect board geometry, component supply and soldering requirements within the same manufacturing discussion.

  • PCB and assembly support through one supplier. A small land-pattern or board-layout issue can affect 0201 soldering. Having fabrication and assembly services together gives your team one point of coordination for discussing those interactions.
  • Procurement through manufacturers and authorized distributors. Our sourcing service supports BOM-based purchasing, including the exact device and package required by the design. This is particularly relevant when miniature parts have similar descriptions but different ratings or dimensions.
  • Equipment for small-component assembly and inspection. Our SMT capability extends down to 01005, with SPI and AOI available at their respective process stages. For 0201 builds, this supports examination of both the printed deposit and the finished placement.
  • Supply options that fit existing inventory. Full turnkey, partial turnkey and consignment arrangements let you combine our manufacturing support with components or boards already held by your team.

For a new design, these services bring the board, materials and assembly questions into the quotation early. For an existing product, they provide a way to discuss repeat supply around the established BOM, layout and testing requirements.

FAQs About Our 0201 PCB Assembly Services

Can you accept cut-tape 0201 components for a prototype order?

Cut tape is among our supported component supply formats. Feeder compatibility, tape condition, usable leader length and the quantity available for setup need to be reviewed for the specific parts. Include the packaging format when requesting a consignment quotation.

Can 0201 components be assembled on both sides of a PCB?

Yes, double-sided SMT can include 0201 parts. The assembly sequence must account for the second thermal cycle, first-side component retention and support for the board during processing.

Does every 0201 assembly require nitrogen reflow?

Nitrogen is a process option whose value depends on the solder paste, surface finish and wetting behavior. The 0201 package designation alone does not establish that it is required. The atmosphere should be selected with the complete soldering process.

Can 0201 components be hand-soldered or reworked?

Skilled technicians can work on 0201 parts with suitable magnification and controlled tools. Closely spaced neighboring components and small pads make access and heat control important. A repaired location may also require cleaning, inspection and electrical retesting.

Can a 0402 component be replaced by a 0201 equivalent without changing the PCB?

A smaller replacement requires evaluation of both the footprint and electrical specifications. Matching resistance or capacitance alone is insufficient. Voltage rating, power capability, temperature behavior and termination fit can differ, so a footprint revision may be necessary.

Are additional components needed for a consigned assembly order?

Setup, handling and potential replacement needs can require parts beyond the exact fitted quantity. The allowance depends on packaging, component type and batch size. It should be agreed during quotation, especially when only a limited quantity of an expensive or scarce part is available.

For your next 0201 PCB assembly project, email sales@bestpcbs.com with your board files, BOM and required quantities. Tell us whether you need a prototype build, repeat production or a combined supply plan, and we can review the assembly and quotation requirements with you.

You may also like

Fine Pitch PCB Assembly Services in China for QFP, QFN and BGA

November 2nd, 2026

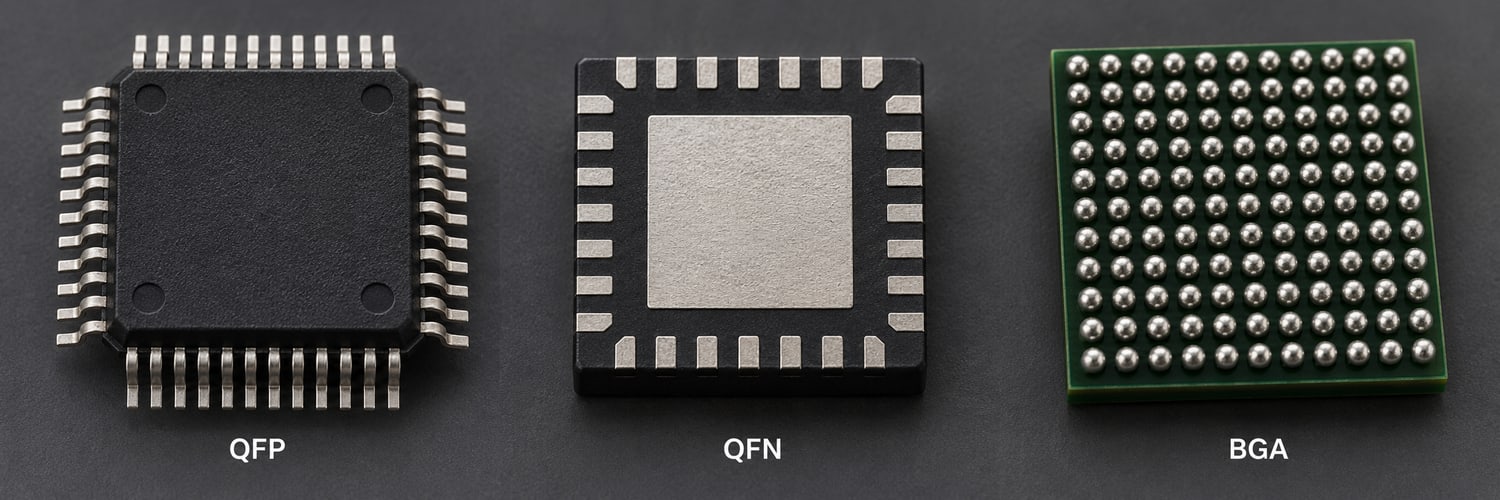
Fine pitch PCB assembly requires a different inspection plan for a QFP than for a BGA, even when their leads or balls have the same center-to-center spacing. A camera can see a lifted QFP lead. Inspecting the inner rows of a BGA requires a view beneath the package.

At EBest Circuit, we coordinate PCB fabrication, component sourcing, assembly and testing for prototypes and repeat orders. Send the part number of your tightest-pitch device, the board files and your build quantity to sales@bestpcbs.com for a footprint review and quotation.

fine pitch PCB assembly

Top 10 Fine Pitch PCB Assembly Service Providers in China

These ten providers offer fine-pitch assembly in China. They are listed alphabetically. For a useful shortlist, start with the package you need assembled and the type of order each provider handles.

Provider Assembly focus
BELI Technologies Turnkey or consigned; 0.4 mm BGA pitch
EBest Circuit (Best Technology) Rigid and specialty boards; turnkey assembly and test
JLCPCB BGA pitch: 0.3 mm Standard; 0.5 mm Economic
NextPCB Prototypes and small batches; BGA X-ray
OurPCB QFN, BGA and CSP; stencil review
PCBasic Prototype to volume; BGA inspection and rework
PCBONLINE Fine-pitch IC prototypes; stencil design
PCBSINO Short runs; mixed SMT and through-hole assembly
Saturn PCBA 0.25 mm pitch BGA; box build
Shenzhen BangYan Electronic Technology Fine-pitch QFP/QFN; micro-BGA and CSP

A service tier can change the shortlist. For example, a 0.4 mm pitch BGA fits JLCPCB’s Standard spacing limit but falls below its Economic limit. For comparable quotes, give each provider the same part number, board revision and test requirements.

EBest Circuit’s Fine Pitch PCB Assembly Services Across Board Types

We match the tooling and soldering process to the board construction. The same fine-pitch component may need different support on flex and a different reflow profile on a metal-core board.

  • Rigid FR-4 and HDI. Before fabrication, we review the BGA lands, solder-mask openings and via treatment together. An open via in a pad can draw solder away from the joint.
  • Flexible PCB. A carrier holds the component area flat during printing and placement. Stiffener position matters: flex that moves under the stencil can receive uneven paste deposits.
  • Rigid-flex PCB. We support the populated rigid sections while leaving clearance at the flex transitions. The panel drawing shows where the fixture can contact the board without loading a bend.
  • Metal-core PCB. The metal base draws heat away from the pads. We profile the populated board so small ICs and larger thermal pads can solder within the paste and component temperature limits.

Our Fine Pitch SMT Assembly Capabilities for QFP, QFN and BGA

We run four SMT lines: two JUKI and two Yamaha. For a board containing a fine-pitch BGA and small passives, two separate limits matter.

Feature Capability
Smallest passive package 01005
Minimum BGA ball pitch 0.25 mm, subject to package review
Paste printing GKG-GLS; 0.022 mm nominal accuracy
Placement Yamaha YRM20; 0.025 mm nominal accuracy
Reflow Ten-zone nitrogen oven; board profiling

BGA pitch is the distance between ball centers. It is distinct from ball diameter and from the placement machine’s accuracy. We review the actual part drawing before accepting a build at the pitch limit.

  • QFP leads. A bent lead can sit above the paste even when the body is centered. We check lead alignment, bridges and lifted leads.
  • QFN exposed pad. Excess paste beneath the center pad can lift the package and leave perimeter terminals open. We review the center and perimeter apertures together.
  • BGA ball array. We match the lands and stencil to the ball pattern, check the thermal profile on the board and use X-ray to inspect hidden joints.

If your board also includes wafer-level packages, our WLCSP assembly guide covers pad design, stencil openings and hidden-joint inspection.

fine pitch PCB assembly

Fine Pitch Assembly Lead Times for Prototypes, Small Batches and Repeat Orders

For qualifying orders, we offer a 1.5-week PCBA turnaround covering fabrication, assembly and agreed testing. The quote confirms the starting point and ready-to-ship date after we review files, parts availability and test preparation. Freight transit is separate.

  • First prototype. Allow for footprint review, board fabrication, stencil preparation and first-article checks. A new flex carrier or functional test fixture can set the earliest start date.
  • Small batch. An approved prototype can save setup time if the stencil, placement program and profile remain valid. A new package suffix or panel layout may require a fresh review.
  • Repeat order. With the revision unchanged, component availability, line scheduling and test throughput usually determine the ship date.

If you supply the processor, its arrival can set the start of assembly even when the bare boards are ready. If you need engineering samples ahead of the main lot, include both dates in the RFQ so we can assess a split shipment.

Our Quality Control for Fine Pitch Assembly: SPI, AOI and X-Ray Inspection

We inspect the paste before placement, the visible joints after reflow and the hidden joints by X-ray. For a BGA that must also pass an electrical or functional test, we agree on coverage separately.

Method Inspection or test focus Coverage limit
3D SPI Paste volume, height and offset Before placement only
AOI Orientation, bridges and lifted leads Visible features only
X-ray Hidden bridges, ball offset and voids Geometry, not electrical continuity
ICT Opens, shorts and component values Accessible, programmed test nodes
FCT Powered operation under defined loads Agreed functions and limits

A row of offset QFP paste deposits can be flagged before any IC is placed. For an intermittent fault under a BGA, a normal X-ray image alone cannot establish good wetting or electrical contact. Our team can use the electrical findings alongside inspection results and MES batch records to narrow the investigation.

fine pitch PCB assembly

Fine Pitch PCB Assembly Case Study: A Medical Board with a 0.3 mm Pitch BGA

A medical device manufacturer needed a motherboard assembled with a 0.3 mm pitch BGA and 0201 passives. Once the BGA was placed, optical inspection could no longer show the internal ball rows.

  1. Footprint review. Our engineers recommended adjusting the BGA pad dimensions before fabrication.
  2. Material handling and placement. We purchased components through authorized distributors, controlled moisture-sensitive parts and aligned the BGA using the Yamaha YSM20R vision system.
  3. Verification. We inspected every BGA on this build by X-ray, then tested board functions under simulated operating conditions.

The two checks answered different questions for the customer: X-ray examined the solder array; the powered test verified the functions exercised by the procedure.

Why Choose EBest Circuit as Your Fine Pitch PCB Assembly Supplier?

Working with EBest gives your team one contact for the bare board, the component kit and the tested assembly. That coordination matters most when a small change affects all three.

  • Footprint review before parts are bought. If a replacement IC has the same pin count but a different package suffix, we check the land pattern, stencil and placement data before submitting the alternate for your approval.
  • Control over critical parts. Supply an allocated processor and let us purchase the rest of the BOM, or assign the complete kit to us under a turnkey order.
  • Inspection matched to acceptance. If your customer needs BGA images or a powered I/O test, we agree on coverage, fixtures and records at quotation so the deliverables are clear before production.
  • Continuity on repeat orders. We compare the new release with the approved BOM, panel and test revision. Unchanged tooling can be reused where appropriate; changes are reviewed before the line is set up.

For an itemized quote, send the Gerber or ODB++ files, BOM, placement data, assembly drawing and critical package drawing. Include initial and repeat quantities, your target date and any inspection records you need.

Fine Pitch PCB Assembly FAQs

Can I supply only the BGA processor and have EBest source everything else?

Yes. In a partial turnkey order, identify the consigned processor by part number and quantity. We review its packaging, moisture condition and expected arrival alongside the parts we will procure.

Can you use cut tape or trays for a short prototype run?

We can review reels, cut tape, tubes and trays. For a short strip of expensive fine-pitch parts, confirm the feeder setup and handling allowance before sending exactly one component per board.

Can an existing stencil be reused after a PCB revision?

Possibly. We compare the revised paste and pad data, panel layout and tooling alignment with the existing stencil. Even if the schematic is unchanged, a revised thermal pad or shifted panel origin can require new tooling.

Do you need firmware for functional testing?

Only if the agreed functions depend on it. For a programmable board, provide the released firmware version, programming instructions, expected responses and pass/fail limits. A basic power-up check and a full I/O test are different quotation items.

Can X-ray images or inspection reports ship with the boards?

Specify the reference designators, sampling level and record format when requesting the quote. Inspection performed on the line and a customer-specific report are separate deliverables.

Can you assess a BGA if I know only its ball diameter?

Send the full manufacturer part number or package drawing. Ball diameter alone does not give the center-to-center pitch, array layout or required PCB pad geometry, so it is insufficient to approve the assembly.

At EBest Circuit, we use 3D solder paste inspection to check paste deposits before placing fine-pitch components. After reflow, we use optical inspection for exposed QFP leads and X-ray inspection for hidden BGA joints. For a fine pitch PCB assembly quotation, email sales@bestpcbs.com with your smallest-pitch part number, board quantity and target delivery date. Include the test or inspection record your customer needs for acceptance.

You may also like

PCB Assembly Outsourcing with No MOQ and Fast Turnaround

October 30th, 2026

PCB assembly outsourcing can free your OEM team from coordinating a bare-board supplier, component orders and an assembly shop separately. At EBest Circuit, PCB fabrication and PCBA assembly are connected from the manufacturing review onward, so panel design, material availability, soldering and testing are planned around the same released product. You can start with the quantity needed for validation and continue into repeat production without rebuilding that supplier coordination for each stage.

Our manufacturing support combines four SMT lines, 01005 placement, fine-pitch BGA assembly, nitrogen reflow and MES single-board traceability. No MOQ makes small builds practical, while a 1.5-week PCBA delivery option is available for suitable, fully assessed projects. Send your PCB files, BOM, quantity and target date to sales@bestpcbs.com for a quotation and a production plan matched to your build.

PCB assembly outsourcing

Turnkey PCB Assembly with Flexible Sourcing Options

Our own PCB and PCBA facilities allow fabrication and assembly decisions to be reviewed together. Panel rails and fiducials can be planned before the bare boards are made; component packages can be checked against footprints before purchasing. This reduces the chance that your team receives finished PCBs that need modification before assembly can begin.

The sourcing model can fit your existing purchasing arrangements. You can hand over the complete BOM, retain selected strategic components, or supply an agreed kit.

Supply Model Component Supply Customer Purchasing Role
Full turnkey EBest sources the approved BOM Approve specifications and proposed alternatives
Partial turnkey Customer parts plus EBest procurement Supply selected or proprietary components
Consigned assembly Customer supplies the agreed kit Retain component purchasing control

PCB fabrication can be included with full or partial turnkey work. For consigned assembly, the order specifies whether you supply the bare boards or we manufacture them.

Our component sourcing team checks manufacturer part numbers, availability, package format and quantities against the assembly requirements. Procurement through manufacturers and authorized distribution channels supports source traceability. If a part is unavailable, an alternative is submitted with the relevant specifications for your approval before use.

Customer-supplied and purchased parts are coordinated as one production kit. A missing connector, an incompatible package or an unapproved substitute is therefore addressed within the manufacturing project, rather than passed between separate purchasing and assembly suppliers. Your engineers retain approval of product changes while our team handles the material and production follow-up.

Programming, cable installation and enclosure assembly can also be included. Carrying these requirements into the initial project review helps align connector access, board mounting and test preparation before final integration.

PCB Assembly Services Across Board Types

EBest Circuit's board range allows an OEM to place different PCB constructions with one manufacturing contact. A product may combine an FR4 controller, a flexible interconnect and an LED board; each needs its own fabrication and assembly approach, but the purchasing and engineering coordination can stay within one project.

  • FR4 and high-Tg boards. Single-sided, double-sided and multilayer builds are reviewed for material, stackup, surface finish and assembly requirements. High-Tg material is selected against the design and thermal-process requirements, rather than treated as a substitute for product-level thermal validation.
  • HDI boards. Fine-pitch footprints, microvias and solder-mask features are considered together. Addressing the pad and via structure before fabrication helps avoid soldering problems that would be expensive to correct after components are purchased.
  • Heavy copper boards. Large copper areas and power connections draw heat differently during soldering. Fabrication requirements and the thermal demands of the populated board are reviewed together, including through-hole connections where present.
  • FPC and rigid-flex boards. Stiffener locations, panel support and populated areas are considered before assembly. This helps keep flexible circuits supported during printing and placement while preserving the intended flexible sections.
  • Metal-core PCBs. Aluminum- and copper-core constructions serve LED and power designs. Dielectric requirements, mounting geometry and the board's heat-transfer behavior are considered alongside component placement and soldering.

This range is useful when your product family contains more than one board technology. You can coordinate related boards through the same team while each follows its appropriate manufacturing route. Dimensions, copper weights and fine-feature limits are evaluated for the particular construction; they are not assumed to be identical across factories or board types.

Contract PCB Assembly for SMT and Through-Hole Projects

Four SMT production lines—two JUKI and two YAMAHA—give our production team options for matching a build to its component mix, feeder requirements and available line capacity. For an OEM with engineering samples and recurring orders, that supports scheduling around the actual assembly work, including small passives, fine-pitch devices and larger components.

Process / Feature Specification
SMT line configuration Four lines: two JUKI, two YAMAHA
Minimum SMD package 01005 component placement
Minimum BGA pitch 0.25 mm, subject to package review
Assembly technologies SMT, through-hole and mixed assembly
Reflow soldering Nitrogen reflow capability
Through-hole soldering Wave and selective wave soldering
Component presentation Reels, cut tape, tubes, trays, loose parts

For 01005 components, the manufacturing work starts with the paste deposit and component presentation. Stencil openings, paste selection, feeder consistency and placement setup all affect whether these small parts solder correctly. Nitrogen reflow helps limit oxidation and improve wetting where required by the process. These controls make small-component capability relevant to a complete build, rather than an isolated placement specification.

Fine-pitch BGA assembly also requires control beneath the package. The land pattern, stencil, board support and thermal profile must suit the device. X-ray inspection can then examine joints that cannot be evaluated by surface inspection alone. The process is selected for the assigned line and package; the minimum pitch is not a blanket approval for every BGA design.

For boards combining SMT devices with connectors or other through-hole components, wave and selective wave soldering provide different production routes. Selective soldering can target accessible through-hole joints where the layout permits, helping accommodate populated SMT areas nearby. Planning the soldering sequence and tooling together reduces the need to treat the through-hole work as a separate job after SMT is complete.

PCB assembly outsourcing

PCB Contract Manufacturing with Certified Quality and Traceability

Quality control needs to catch process problems early and leave enough evidence to investigate the assemblies later. Our inspection, testing and traceability capabilities address both needs, from paste printing through finished-board verification.

Inspection at the stage where defects arise

SPI, including 3D SPI, checks paste volume, height and position before components are placed. This creates an opportunity to address printing defects before they become solder-joint problems. AOI checks visible assembly features after soldering; DIP AOI extends optical inspection to applicable through-hole work. X-ray addresses hidden joints, including those beneath BGA packages.

Electrical verification is planned separately. ICT can check accessible circuit nodes and component-related conditions, while FCT exercises the board using defined inputs, firmware and acceptance limits. For example, an LED operation check and a controller test covering interfaces and operating modes require different fixtures and procedures. We define the required coverage with the project so the test effort corresponds to what your product needs verified.

MES records that help narrow an investigation

Our MES supports single-board tracking and five-second retrieval of relevant recorded material, product-batch and production information. These records help connect an individual assembly with its manufacturing history and production status.

If an investigation concerns a component lot, the associated records help identify which boards or batches require review. If the issue appears after a repeat build, production history can be reviewed alongside the applicable inspection and test records to investigate differences between batches. This gives your quality team a more focused starting point than reconstructing the build from scattered emails. The five-second capability refers to record retrieval; diagnosis and corrective action depend on the issue.

Certification matched to the manufacturing scope

EBest Circuit's quality-system credentials include ISO 9001, ISO 13485, IATF 16949 and AS9100D. Their relevance differs across general manufacturing, medical, automotive and aerospace programs, so the applicable certificate is matched to the manufacturing entity, site and activity involved in the order.

For your supplier qualification, the useful evidence combines that certificate scope with the product's manufacturing requirements, material traceability and agreed inspection records. Certification supports the quality system; the production records demonstrate how the requirements were addressed for the particular build. This connection also helps maintain continuity when a prototype becomes a recurring order.

PCB assembly outsourcing

Low Volume PCB Assembly with No MOQ

EBest Circuit accepts small PCBA orders with no minimum order quantity, giving you access to PCB fabrication, component sourcing, precision assembly and testing without a large-volume commitment. Order quantity does not limit you to basic assembly services; the manufacturing and inspection scope is matched to your board's requirements.

Complete manufacturing for small orders

Our PCB and PCBA facilities coordinate bare-board fabrication, material preparation and SMT/DIP assembly within one project. Full Turnkey, Partial Turnkey and Consigned Assembly options let us procure the complete BOM, source selected parts or work with your supplied kit. Small orders can therefore include the same range of manufacturing services needed to deliver tested hardware, rather than leaving you to arrange fabrication or testing separately.

Precision assembly backed by inspection and testing

Four SMT lines—two JUKI and two YAMAHA—allow our team to match small builds to the component mix and required production setup. Relevant capabilities include:

  • 01005 placement and 0.25 mm BGA pitch. Support for compact, densely populated boards, subject to package and process review, with nitrogen reflow available to support solder wetting.
  • SPI, including 3D SPI, AOI and X-ray. Inspection options address paste deposits, visible assembly features and hidden solder joints, so small quantities can receive inspection appropriate to their assembly risks.
  • ICT and FCT. Project-specific electrical testing can be included with agreed access, fixtures, programs and acceptance criteria, giving you verification beyond visual inspection.

These capabilities are available to low-volume projects; the inspection and test plan determines which processes your build needs.

Traceable builds with a quick-delivery option

MES single-board traceability supports five-second retrieval of relevant recorded material, batch and production information. Even a small build has a manufacturing history that can support quality investigations. For repeat orders, existing production records can be reviewed alongside the approved PCB revision, BOM and test requirements to prepare the next build.

A 1.5-week PCBA quick-delivery option is available for suitable projects after review of released files, material availability, assembly complexity and testing requirements. Required fixtures, firmware and test programs must be ready for the agreed schedule; the quotation specifies its starting point and scope, with transit and customs addressed separately.

Component pack sizes, supplier minimum purchases and setup charges still apply where relevant. These are identified in the quotation so the cost and material commitment remain clear even when the assembly quantity is small.

PCBA Contract Manufacturing: A Real Project Case Study

For a UK surgical-lighting project, EBest Circuit handled an aluminum-core LED PCB and its associated component procurement and assembly. The order called for 150 assemblies plus one spare, with manufacturing requirements extending beyond LED placement to mounting-hole position, cleaning and operation checks.

The PCB specification was a single-sided aluminum-core construction, 1.6 mm ±10% thick, with 1 oz copper, a lead-free tin finish, black solder mask and gray legend. The production panel and stackup required customer approval before fabrication.

Three manufacturing priorities

  • Panel and assembly coordination. The bare-board and SMT orders were linked, with all components procured by EBest Circuit. Panel delivery was permitted, allowing the fabrication arrangement to remain compatible with downstream handling.
  • LED and mounting alignment. The production instructions emphasized accurate LED placement and optical measurement of hole positions. This addressed two separate fit requirements: locating the light-emitting components correctly and preserving the board's mounting geometry.
  • Cleanliness and operation. The order required board washing, removal of solder balls and rosin or other residue, and checks that every LED operated before shipment.

The customer obtained PCB manufacturing, component purchasing and completed PCBA work through one project, with the mechanical and inspection requirements carried into the assembly instructions. That integration is the manufacturing value of the case: the OEM did not need to transfer bare boards and a separately purchased component kit between suppliers or restate the mounting and cleanliness requirements at each handoff.

PCB Assembly Cost and a Project-Specific Quote

EBest Circuit helps control total PCBA project cost by coordinating PCB fabrication, component sourcing, SMT/DIP assembly, testing and box build before production begins. Your team works through one manufacturing contact, reducing supplier handoffs while our engineers review how panel design, materials and production preparation affect the complete build cost.

Coordination Area Cost-Control Value
Panel design and assembly handling Avoid incompatible panels and extra tooling
BOM availability and approved alternatives Assess purchase and validation costs together
Stencils and production setup Identify reusable preparation for repeat builds
Programming and test requirements Define fixtures and coverage before production

A panel layout is reviewed for both bare-board utilization and assembly support, so material savings do not create avoidable handling costs. Proposed component alternatives require your approval, with package compatibility and any additional validation considered before purchasing. This joint review helps address changes while they can still be incorporated into the production plan.

Sourcing that fits your purchasing arrangements

  • Full Turnkey. Assign BOM purchasing and production coordination to EBest, reducing the separate orders and material follow-up your team manages.
  • Partial Turnkey. Retain selected parts under your existing supply agreements while we procure the remaining BOM and coordinate the combined kit.
  • Consigned Assembly. Supply the agreed component kit to use your own purchasing channels or available inventory; bare-board supply is agreed separately.

The best fit depends on stock, purchasing terms and material readiness. We assess those conditions with the assembly requirements rather than assuming one supply model always costs less.

Quote development quantities and repeat orders together

No MOQ lets you order the prototype quantity you need without committing to a large PCBA batch. Providing anticipated repeat quantities also lets us evaluate component purchase breaks, packaging quantities and how stencil and setup charges affect each build. Supplier minimum purchases still apply where relevant; potential tooling reuse is assessed against the approved design and production requirements.

For an accurate quotation, send Gerber or ODB++ files, the fabrication specification, BOM with manufacturer part numbers, CPL/pick-and-place data and assembly drawings. Add prototype and repeat quantities, the target date, sourcing model and programming or test instructions. Include enclosure and wiring requirements for box build assembly.

Our quotation identifies PCB fabrication, component procurement, stencils and production preparation, assembly, inspection and testing, plus any required box build, packing or logistics charges. One-time costs, material purchase quantities, supply constraints and the proposed schedule are made clear so you can plan both the immediate order and subsequent builds. If files are incomplete, an initial assessment identifies what is needed before a production quotation can be finalized.

FAQs About PCB Assembly Outsourcing

Can we provide firmware and an existing test fixture?

Yes. Customer-provided firmware, programming instructions and fixtures can be reviewed for the build. Connections, software versions, operating limits and pass/fail criteria are established before the test setup is used in production.

What happens to unused customer-supplied components?

Return or retention is agreed with the order. Remaining parts can be returned with the assemblies or retained for a future build under the agreed arrangement. The initial kit also needs sufficient material for setup and handling.

Can some component positions be left unpopulated?

Yes. Mark do-not-populate positions consistently in the BOM and assembly instructions. This distinguishes an intentional product variant from a missing component and keeps the assembly and inspection requirements aligned.

Can conformal coating or potting be included?

These operations can be evaluated with the PCBA. Material, coverage, keep-out areas, curing and inspection requirements are defined together, with programming and relevant testing planned before access to the board is restricted.

Can you quote the PCBA together with enclosure assembly?

Yes. Mechanical drawings, wiring details, connector requirements and the final test procedure allow the enclosure work to be quoted with the board. This helps address mounting, cable access and complete-unit testing before assembly begins.

Can we change the design between the prototype and the next order?

Yes. The next build uses the approved new release. Our review identifies the effect on purchased materials, stencils, assembly preparation, firmware and tests, so the revised order does not unintentionally inherit obsolete requirements.

EBest Circuit coordinates PCB fabrication, component sourcing, SMT/DIP assembly, testing and box build within one PCB assembly outsourcing project, with four SMT lines—two JUKI and two YAMAHA—to accommodate different component mixes and build requirements. SPI, AOI and X-ray inspection, together with project-specific electrical testing and MES single-board traceability, help control production quality and keep records accessible for batch reviews and quality investigations. To put these capabilities to work on your build, send your files, quantity and target date to sales@bestpcbs.com. We will review your requirements and return a project-specific quotation with the manufacturing scope and proposed schedule.
You may also like

Motion Sensor PCB Manufacturing & Assembly for Reliable Detection

October 30th, 2026

A motion sensor PCB can pass electrical testing yet still produce false triggers, unstable readings, or inaccurate detection results. Electrical interference, sensor placement, and assembly stress are common sources of problems that basic PCB testing may not reveal.

Whether you’re developing a PIR motion sensor light, a MEMS motion tracking device, or a wireless detector, you need a manufacturer that can handle the PCB fabrication, sensor assembly, and testing requirements of your design. Understanding these requirements early can help you avoid production delays, unexpected costs, and reliability problems.

motion sensor PCB, https://www.bestpcbs.com/blog/2026/10/motion-sensor-pcb/

Are you worried about your motion sensor PCB project?

  • False triggers after assembly: Noise, mounting stress, unstable power, or enclosure effects can change sensor behavior even when basic electrical checks pass.
  • Unclear test coverage: AOI and continuity testing cannot prove detection range, sensor orientation, firmware behavior, or wireless performance.
  • Cost and schedule surprises: Sensor availability, fine-pitch assembly, programming, fixtures, and calibration can change the quotation and lead time.

Which Type of Motion Sensor PCB Is Right for Your Application?

Choosing the right motion sensor PCB starts with what your product needs to detect. PIR, microwave, ultrasonic, and MEMS sensors work differently, and each places different demands on the PCB.

motion sensor PCB, https://www.bestpcbs.com/blog/2026/10/motion-sensor-pcb/

Motion Sensor PCB Type Applications Key PCB Requirements
PIR Motion Sensor PCB Motion sensor lights, security alarms Low-noise analog circuits, stable power, optical alignment
Microwave Motion Sensor PCB Smart lighting, automatic doors RF layout, antenna clearance, grounding
Ultrasonic Motion Sensor PCB Proximity detection, automated equipment Transducer connections, driver circuits
MEMS Motion Sensor PCB Wearables, robotics, sports monitoring Compact SMT assembly, sensor orientation, mechanical stability

Wireless communication can be added to any of these systems using Bluetooth Low Energy, Wi-Fi, or another suitable radio technology. The sensing method and communication interface should be selected independently to match the intended application.

What Should You Consider Before Designing a Custom Motion Sensor PCB?

A custom motion sensor PCB needs to meet the product’s detection, electrical, mechanical, and assembly requirements. Addressing the following factors during design can prevent problems that become expensive to correct after production begins.

  • Detection Requirements: For PIR applications, establish the detection range, coverage angle, response time, and acceptable false-trigger behavior. MEMS applications require defined measurement ranges, sensing axes, sampling rates, and accuracy targets. These specifications help determine the sensor IC and supporting circuitry.
  • PCB Structure and Component Placement: Select the layer count, board dimensions, thickness, and mounting locations to suit the enclosure. Keep MEMS sensors away from areas subject to excessive bending or mounting stress. PIR sensors also need proper alignment with the optical lens and intended detection field.
  • Power Management: Battery-powered motion sensors need low standby current and stable voltage regulation. Wireless devices may draw brief current peaks during transmission, so the power distribution and decoupling must prevent these changes from disturbing sensitive sensor circuits.
  • RF and Antenna Layout: Microwave sensors and wireless modules need suitable antenna clearance, grounding, and RF routing. Batteries, metal enclosures, and nearby copper can affect antenna performance. Follow the module manufacturer’s reference layout and check the antenna arrangement in the finished product.
  • Sensor Package Compatibility: Check component footprints, soldering limits, moisture sensitivity, and availability before finalizing the BOM. MEMS devices in LGA packages may need specific land patterns, stencil openings, and reflow conditions to avoid poor solder joints or excessive package stress.
  • Programming and Test Access: Include accessible points for power measurements, programming, communication signals, and relevant sensor outputs. Without adequate test access, production may require more complex fixtures, increasing test time and cost.

A design that accounts for these requirements is easier to manufacture, assemble, and verify without unnecessary revisions.

How Can You Reduce Signal Noise and False Triggers in a Motion Sensor PCB?

Reducing signal noise starts with the PCB layout, power supply, sensor mounting, and signal-processing circuit. The causes of unstable readings vary between PIR, MEMS, and microwave sensors, so the solution must match the problem.

motion sensor PCB, https://www.bestpcbs.com/blog/2026/10/motion-sensor-pcb/

  • Minimize Interference in PIR Circuits: PIR sensors generate weak signals that can be affected by nearby electrical noise. Keep sensitive analog traces away from switching regulators, relay drivers, and high-current paths. Proper grounding, local decoupling, and signal filtering help reduce interference at the sensor input.
  • Optimize Signal Amplification and Filtering: Increasing amplifier gain also increases unwanted noise. Choose gain, bandwidth, and detection thresholds that suit the expected motion signal. Test the complete signal chain to confirm that the required sensitivity is maintained without excessive false triggering.
  • Reduce Mechanical Stress on MEMS Sensors: PCB bending, mounting pressure, and soldering stress can change accelerometer or gyroscope readings. Follow the sensor manufacturer’s footprint and reflow recommendations, support the PCB during assembly, and avoid placing sensitive devices in areas of concentrated strain.
  • Maintain Stable Power and Temperature Conditions: Voltage fluctuations during wireless transmission or output switching can disturb sensor operation. Use appropriate regulation and decoupling, and keep significant heat sources away from temperature-sensitive sensors. Check performance across the intended voltage and temperature range.
  • Improve RF Layout and Antenna Performance: Microwave sensors and wireless modules require suitable antenna clearance, grounding, and routing. Metal components, batteries, and enclosure materials can influence RF behavior. Verify the antenna arrangement using the actual product enclosure rather than relying on PCB-level testing alone.
  • Control SMT Assembly Quality: Component misalignment, uneven solder joints, and unsuitable reflow conditions can introduce electrical or mechanical problems. Controlled solder paste printing, component placement, and reflow processes help limit these defects. MEMS packages should be handled according to their specific assembly requirements.
  • Test Under Real Operating Conditions: Evaluate PIR devices for unwanted triggers related to temperature changes, airflow, and environmental movement. For MEMS products, check measurement stability under expected vibration and mounting conditions. Wireless devices should also be tested during radio transmission and changes in power demand.

PCB manufacturing and assembly controls address many sources of interference and measurement error. Firmware settings, calibration, optical design, and environmental conditions must also be considered when evaluating the finished product.

What Does a Custom Motion Sensor PCB Manufacturing & Assembly Service Include?

EBest Circuit provides PCB fabrication, component sourcing, SMT/THT assembly, inspection, and testing services for custom motion sensor PCB projects. Full-turnkey, partial-turnkey, and consigned assembly options allow customers to select the manufacturing scope that fits their needs.

  • Free DFM & Engineering Review: Review Gerber files, PCB stackup, component footprints, BOM, and assembly drawings before fabrication. Identify potential problems involving sensor placement, solder pads, clearances, and manufacturability.
  • Custom PCB Fabrication: Manufacture single-sided, double-sided, multilayer, and HDI PCBs using materials, copper thicknesses, and surface finishes suited to the approved design. Standard FR4 construction and finer routing processes are available for different circuit requirements.
  • Component Sourcing: Source approved PIR sensors, MEMS devices, microcontrollers, wireless modules, connectors, and passive components. Check availability and confirm any proposed substitutes with the customer before purchasing.
  • Precision SMT & THT Assembly: Support single-sided and double-sided SMT, fine-pitch QFN, LGA, BGA, and miniature SMD packages, as well as through-hole and mixed-technology assemblies. Solder paste printing, placement, and reflow conditions are selected to suit the component requirements.
  • Quality Inspection & Functional Testing: Provide SPI, AOI, X-ray inspection, and electrical testing where applicable. Firmware programming, sensor output verification, and application-specific functional testing can be arranged when the necessary procedures and fixtures are available.
  • Prototype to Mass Production: Support initial prototypes, pilot builds, and volume orders using approved design revisions and BOMs. Production schedules and quality requirements are confirmed against the components and manufacturing processes involved.

How Can You Verify Motion Sensor PCB Quality and Detection Performance?

A motion sensor PCB needs both manufacturing inspection and functional testing. A board may pass electrical continuity checks and assembly inspection without meeting its sensing requirements.

motion sensor PCB, https://www.bestpcbs.com/blog/2026/10/motion-sensor-pcb/

The following tests address different aspects of PCB and PCBA quality:

  • PCB Electrical Testing: Check bare boards for open circuits, short circuits, and incorrect connections before assembly. This confirms the required electrical connections but does not establish sensor functionality.
  • SMT Assembly Inspection: Use SPI to check solder paste deposits and AOI to identify visible placement errors, polarity problems, and soldering defects. X-ray inspection can examine selected hidden solder joints beneath LGA, QFN, and BGA packages.
  • Power Supply and Current Testing: Measure supply voltages, startup behavior, standby current, and active current. Battery-powered wireless sensors should also be checked during sensing and radio transmission, when current demand may change significantly.
  • PIR Motion Sensor Testing: Verify sensor response, switching output, and response time under defined conditions. Specify the target, detection distance, movement, sensor orientation, and lens configuration so the results can be reproduced.
  • MEMS Motion Sensor Testing: Check I2C or SPI communication, sensing-axis orientation, output data, and stationary offset. Applications requiring higher measurement accuracy may need calibrated equipment to verify sensitivity and response against approved tolerances.
  • Microwave Motion Sensor Testing: Check detection response, output switching, and current consumption. Detection coverage and sensitivity should be evaluated with the intended antenna arrangement and enclosure.
  • Wireless Communication Testing: Verify the required Bluetooth, Wi-Fi, or other wireless interface, including device connection and sensor data transmission. Communication range and RF performance require separately defined tests when applicable.
  • Functional Acceptance and Quality Records: Agree on test conditions, measurable pass/fail limits, firmware versions, and required inspection records. Specify whether each test applies to every board or an approved sample quantity.

EBest Circuit can support project-specific PCBA testing based on the agreed requirements. Sensor calibration, controlled detection-range testing, environmental validation, and complete-device testing should be confirmed before production, as these services may require dedicated equipment or fixtures.

What Affects Custom Motion Sensor PCB Manufacturing Cost and Lead Time?

Motion sensor PCB cost and lead time depend on the board construction, sensor availability, assembly complexity, testing requirements, and order volume. Understanding these factors helps buyers compare quotations and avoid unexpected production delays.

  • PCB Construction: Additional layers, fine routing, special materials, and irregular board shapes can increase fabrication complexity. Standard FR4 processes are generally more economical when they satisfy the electrical and mechanical requirements.
  • Sensor Availability: Specialized MEMS devices, restricted part numbers, and limited component stock can extend procurement time. Confirm critical sensor availability before releasing the BOM for production.
  • Assembly Complexity: Fine-pitch packages, double-sided SMT, and special component handling affect setup and processing time. Some sensors also need additional controls during soldering and inspection.
  • Testing Requirements: Firmware programming, calibration, dedicated fixtures, and extended functional tests add work beyond routine assembly inspection. These requirements should be defined before quotation.
  • PCB Panelization: Board dimensions, cutouts, and depaneling methods influence material usage and handling. Suitable panelization can improve production efficiency without compromising the board’s mechanical requirements.
  • Order Quantity: Prototype and volume orders have different setup, purchasing, and scheduling needs. A pilot build may be appropriate when moving from manually assembled prototypes to automated production.
  • Design and BOM Changes: Late revisions can require new stencils, updated placement programs, additional component purchasing, or changes to the test procedure. Finalizing the approved files early helps avoid these delays.

A conventional PIR motion sensor light PCB may have a simpler assembly and test scope than a compact wireless MEMS board with fine-pitch components and calibration requirements. A useful quotation should reflect the complete fabrication, sourcing, assembly, and testing scope rather than the bare-board cost alone.

Motion Sensor PCB Case Study: Dual-PIR Detection for False-Trigger Reduction

Texas Instruments’ TIDA-01069 reference design shows how two PIR sensors and low-power signal processing can be used to reduce unwanted motion detections.

This is a Texas Instruments engineering reference design, not an EBest Circuit customer manufacturing project.

Project Background

The system uses two PIR sensors covering separate detection areas. Powered by a single AAA alkaline battery, it targets low-power applications where false triggering can lead to unwanted alarms or device activation.

Requirements and Challenges

The circuit must acquire weak PIR signals while controlling electrical noise and power consumption. Both sensor channels need suitable positioning, signal conditioning, and dependable data acquisition.

Engineering Solutions

The design combines two PIR sensors, low-power analog circuitry, and signal acquisition. Its implementation highlights several important PCB requirements:

  • Accurate placement and orientation of both PIR sensors.
  • Low-noise analog routing and appropriate signal filtering.
  • Stable power distribution for battery-powered operation.
  • Reliable component connections and assembly quality.
  • Functional verification of both detection channels.

Documented Results

Texas Instruments reports detection sensitivity exceeding 30 feet (approximately 9 meters) under the reference design’s specified test conditions.

The dual-sensor architecture is intended to help distinguish motion events and reduce unwanted triggering. Actual performance depends on the completed design, assembly, and operating environment.

A similar PCB assembly would require its own manufacturing inspection and functional acceptance tests. The reference design’s results do not establish another manufacturer’s production yield or detection performance.

Why Choose EBest Circuit for Motion Sensor PCB Manufacturing & Assembly?

EBest Circuit brings PCB fabrication, component sourcing, SMT/THT assembly, and engineering support together for custom motion sensor PCB projects. Customers can coordinate these services through one manufacturing supplier.

  • Free DFM Review: Receive engineering feedback on PCB construction, footprints, assembly clearances, and potential manufacturing difficulties before production.
  • One-Stop PCB and PCBA Services: Arrange PCB fabrication, component procurement, assembly, inspection, and agreed testing through a coordinated manufacturing process.
  • Engineering Support: Discuss fine-pitch packages, compact board layouts, sensor mounting conditions, and special assembly requirements with the engineering team.
  • Quality Management: EBest Circuit’s public company materials list ISO 9001, ISO 13485, IATF 16949, and AS9100D. Request current certificate copies and confirm the certified site and scope that apply to your order during supplier qualification.
  • Prototype and Volume Manufacturing: Move from initial builds to pilot orders and repeat production using approved design files, BOMs, and manufacturing requirements.
  • Testing and Traceability Support: Define the required inspection methods, functional tests, component records, and production documentation before manufacturing begins.
  • Component Sourcing Assistance: Check availability of critical sensors and coordinate customer-approved alternatives when sourcing constraints arise.
  • Delivery Coordination: Establish production and shipment schedules based on the approved order, component readiness, and required manufacturing processes.

EBest Circuit can review your motion sensor PCB design files and provide a manufacturing and assembly proposal based on the board specifications and project requirements.

FAQs About Custom Motion Sensor PCB Manufacturing & Assembly

Q1: Can I supply my own PIR or MEMS sensors for assembly?

A1: Yes. Customer-supplied components can be considered for partial-turnkey or consigned assembly. Packaging, quantity, part identification, and handling instructions should be confirmed before production.

Q2: Can I order bare motion sensor PCBs without assembly?

A2: Yes. Bare PCB fabrication and complete PCBA assembly are available as separate services.

Q3: Is lead-free soldering available for motion sensor PCB assembly?

A3: Yes, provided the selected components and PCB materials are compatible with the approved lead-free soldering process.

Q4: How are moisture-sensitive MEMS components handled?

A4: Handling follows the component’s moisture sensitivity level, storage requirements, allowable exposure time, and manufacturer instructions.

Q5: Can conformal coating be applied to motion sensor PCBs?

A5: Selective coating may be available after reviewing the component restrictions and masking requirements. Sensor openings, connectors, and coating-sensitive parts must be protected.

Q6: Can assembled motion sensor PCBs be delivered without enclosures?

A6: Yes. Completed PCB assemblies can be supplied separately from lenses, housings, and other mechanical components.

Q7: Can PCB fabrication and assembly be quoted separately?

A7: Yes. Quotations can separate PCB fabrication, component sourcing, assembly, and additional testing according to the requested scope.

How Can You Get a Custom Motion Sensor PCB Quote?

EBest Circuit provides custom motion sensor PCB manufacturing and assembly services for prototypes, pilot runs, and volume orders. Send your Gerber files, BOM, pick-and-place data, assembly drawings, quantity, required delivery date, and delivery location. Include the sensor model, firmware files, and functional test specifications where applicable. Contact sales@bestpcbs.com for a free DFM review, manufacturing feasibility assessment, and quotation.

You may also like

What Causes Tombstoning PCB Defects and How Can You Prevent Them?

October 30th, 2026

Tombstoning PCB defects occur when a small surface-mount component lifts at one end during soldering, leaving that termination disconnected from its pad. The immediate mechanism is an imbalance in the forces acting on the two ends. Preventing the defect means controlling the conditions that create that imbalance, not simply turning the reflow temperature up or down.

Tombstoning PCB defect with one capacitor termination lifted away from its pad

At EBest Circuit (Best Technology), our PCB and assembly services connect board fabrication, stencil preparation, placement and inspection. For a repeated tombstone defect, the useful starting point is the affected reference designator and its two solder joints: what differed before the component lifted?

What Is Tombstoning in PCB Assembly?

PCB tombstoning is a mounting defect in which a two-terminal chip stands on one end or tilts upward like a drawbridge. One termination remains attached while the other loses its intended connection. A fully vertical chip is easy to recognize, but a partially lifted component can also create an open circuit.

The terms Manhattan effect and drawbridge effect describe closely related appearances. A tombstone defect in SMT is not the same as a component that has merely shifted sideways. Inspect its orientation and both terminations before assigning the defect code. Electrical symptoms depend on the circuit: an open series resistor can interrupt a signal, while a disconnected bypass capacitor may leave the product functioning but with inadequate decoupling.

Why Does One End of a Component Lift During Reflow?

Molten solder wets the termination surfaces and applies forces to the chip. If one joint wets before the other, or the forces and their moment arms are unequal, a rotating moment can lift the opposite end. Uneven wetting explains the movement; the investigation must still establish what produced it.

Different solder quantities, pad geometries, termination conditions and heating histories can all contribute. A component photograph shows the final position, not the order in which its joints melted. A recurring lifted end beside a copper plane is a reason to investigate thermal imbalance, not proof that the plane alone caused the failure.

Balanced wetting compared with one end lifting while the other remains soldered

Which Components Are Most Susceptible to Tombstoning?

Small chip resistors and ceramic capacitors are common examples because their low mass offers little resistance to a wetting-force imbalance. 0201 tombstoning and 0402 tombstoning require particular attention to printing consistency and placement overlap. These package names must include their sizing convention: an imperial 0402 is not the same size as a metric 0402.

Imperial / EIA designationMetric designationNominal body length × widthAssembly consideration
040210051.0 × 0.5 mmCheck both termination overlaps and copper connections.
020106030.6 × 0.3 mmSmall absolute print or placement differences become significant.
0100504020.4 × 0.2 mmConfirm package-specific printing, placement and inspection capability.

These are nominal body dimensions, not land-pattern dimensions or acceptance tolerances. Use the exact component drawing for height, termination length and recommended footprint. A tombstoned resistor and a capacitor of the same nominal package need not behave identically; termination construction and solderability also matter. Other two-terminal devices can lift as well, so the diagnosis should follow the actual package rather than assume that all affected parts are capacitors.

Nominal EIA 0402, 0201 and 01005 chip body dimensions

How Do PCB Pads and Copper Connections Affect Tombstoning?

Start with the component manufacturer’s recommended land pattern. Compare pad length, width, spacing and exposed solderable area at the two ends. Oversized or asymmetric pads can change the solder shape and force acting on the terminations. Reducing pad size indiscriminately can trade a tombstone problem for insufficient attachment.

Next compare the copper connected to each pad. One pad tied directly to a broad plane and another connected by a narrow trace may have different thermal responses. Internal copper, nearby vias and the surrounding component population also belong in that comparison. On our FR4 PCBs, this means checking the relevant copper layers, not just matching the two rectangles visible on the top layer.

Matched connections or thermal reliefs may reduce the difference, but they must still satisfy current capacity, grounding and signal requirements. Unfilled vias close to a solderable pad can also disturb the available solder volume. Review the pad, mask opening and via treatment together instead of changing one feature without checking its effect on the others.

Comparison of unequal copper connections and matched connections at a chip footprint

Can Uneven Solder Paste Cause Tombstoning?

Yes. Different paste deposits can leave one termination sitting higher or contacting less paste before reflow. After melting, the unequal solder volumes can also change the joint forces. Examine solder paste volume, height and deposit position as a pair rather than reviewing only the board-wide average.

Aperture blockage, stencil registration, underside contamination and inconsistent release can produce local differences. A nominally symmetric stencil does not guarantee symmetric printed deposits. Our SMT stencil service supports the aperture design needed for the component and board; the printed result still needs verification on the actual assembly.

Reducing excess paste at the outer ends of a chip can be a useful trial when solder volume is the identified contributor. Do not apply a universal aperture reduction to every package. Check the resulting fillets, attachment and printing repeatability, and ensure that a reduction does not introduce opens or poor wetting elsewhere.

How Can Placement Errors Create a Tombstone Defect?

Offset or skew can give the two terminations unequal overlap with their paste deposits. A placement-height error can leave one end without proper contact even when the camera image appears centered. Check the package definition, nozzle condition, pickup, local board support and placement settings for the affected reference designators.

Do not depend on solder self-alignment to correct a chip placed beyond its process tolerance. Equally, increasing placement force without checking the component limits can damage a ceramic body or squeeze paste out of position. Retain the pre-reflow image when possible: it helps separate a chip that was already misplaced from one that rotated during melting.

How Should You Adjust the Reflow Profile to Reduce Tombstoning?

Measure the assembly before changing the oven recipe. The oven-zone setpoints are not the temperature history at the two joints. Compare the affected area with a stable area and assess whether the joints approach melting at different times. On very small chips, sensor size and attachment can perturb the measurement, so profiling needs a suitable instrumented board and a consistent method.

An appropriate preheat or soak can reduce temperature differences, but extending it indefinitely can consume flux activity or exceed a material’s recommended exposure. Keep the profile inside both the selected solder paste window and component limits. A hotter peak cannot repair an unsuitable footprint or unequal paste deposits.

Atmosphere and alloy changes also require a controlled trial. Nitrogen can accelerate wetting, which may aggravate an existing imbalance; it is not automatically a tombstoning cure. Conversely, switching to air may affect other joints on the board. Compare the complete assembly result rather than optimizing only the lifted component.

Which Parameters Should You Record When Investigating Tombstoning?

Record measurements at the affected component, paired with a known-good position or build. The following parameters separate dimensional, printing, placement and thermal contributors. Numerical acceptance limits must come from the selected component, paste and qualified assembly process, not from a generic tombstoning checklist.

ParameterUnit or calculationWhat to recordHow to use it
Body and termination dimensionsmmPart number, package convention, body length/width and termination dimensionsConfirm the correct land pattern and placement definition.
Pad and mask geometrymm; mm²Length, width, gap and exposed area at both endsSeparate drawing symmetry from the actual exposed pads.
Stencil aperture and thicknessmm or µmAperture dimensions, shape, foil thickness and revisionCheck nominal deposit design and local release behavior.
Printed paste volumemm³V1 and V2 from the paired padsCompare individual deposits, not only a board average.
Relative volume difference100 × |V1 − V2| / [(V1 + V2) / 2]Percentage plus the original volumesCompare trials consistently; this formula is not a pass/fail standard.
Paste height and positionµm; X/Y offset in mmBoth deposits and their position relative to padsIdentify unequal seating or print registration.
PlacementX/Y in mm; rotation in degreesActual offset, skew and approved Z-height/force settingsCheck termination overlap before reflow.
Temperature history°C and secondsMeasurement locations, preheat, peak and time above the alloy’s liquidusCompare the actual profile with material limits.
Heating rate°C/sTemperature interval and measurement methodIdentify rapid changes without confusing zone settings with board temperature.
Defect frequencyDefective components / inspected opportunitiesReference designator, panel position, lot and trial sizeCheck whether the corrective action improved repeatability.

For example, illustrative paste volumes of 0.008 and 0.010 mm³ give a relative difference of 22.2% using the formula above. That calculation quantifies the mismatch; it does not establish that 22.2% is an acceptable or unacceptable production limit. Retain the measurement system settings and the absolute volumes when comparing results.

How Do You Find the Root Cause of Repeated Tombstoning?

Start with the distribution of defects. Repetition at one reference designator suggests a different investigation from random defects across many identical chips. A problem confined to one panel edge may involve support, printing or heating conditions. A change coinciding with a new reel, paste lot or stencil revision gives another testable lead.

  1. Preserve the evidence. Record the lifted end, board orientation, reference designator and lot before rework.
  2. Check the pre-reflow condition. Compare paired SPI measurements and placement images.
  3. Compare the design. Inspect pad geometry, copper connections, vias and the component drawing.
  4. Check material and thermal history. Review paste handling, termination condition and the measured profile.
  5. Change one identified factor in a controlled trial. Record the other settings, sample size and defect count.
  6. Verify the full board. Confirm that fewer tombstones did not introduce bridging, insufficient solder or other defects.

AOI can flag component position and visible joint abnormalities, while microscope review helps confirm the physical condition. Electrical testing establishes the resulting circuit behavior but does not identify whether printing, placement or heating caused it. Use the records together; neither a single AOI image nor a passing functional test closes the root-cause investigation.

Tombstoning vs Solder Bridging and Cold Joints: What Is the Difference?

ConditionPhysical distinctionLikely electrical concernInspection focus
TombstoningOne end of the chip lifts from its intended padOpen connection or loss of that component’s functionOrientation and attachment at both terminations
Solder bridgingSolder connects conductors that should be separateUnwanted short circuitClearance and continuity between adjacent nets
Poorly formed or cold jointA joint has not formed properly; the component need not be uprightOpen, high resistance or unstable connectionWetting, joint integrity and process history, not gloss alone
BillboardingA chip rolls onto its narrow sideDepends on termination contact and assembly requirementsBody orientation and the specified mounting condition
Solder grapingFine solder particles remain uncoalesced around a depositJoint-quality concern distinct from chip rotationParticle coalescence and the surrounding joint

A solder bridge in PCB assembly is therefore not another name for a tombstone. Several defects can coexist on the same board, but each needs its own evidence. A dull lead-free joint alone does not prove cold soldering, and an upright component alone does not prove that the reflow peak was too low.

How Do You Repair a Tombstoned Component?

Use an approved rework method compatible with the component and PCB. First isolate the board from power, follow ESD controls and inspect the chip, pads and nearby parts. A cracked body, damaged termination or lifted land needs disposition rather than simply pushing the component flat.

For a reusable component, the rework process must release it without mechanical force against solid solder, restore a suitable solder amount, and position both ends correctly. Replacement is appropriate when component integrity is uncertain or the assembly requirements demand it. Heating tools, preheat and exposure limits depend on the actual package and board.

After rework, inspect both joints and check the relevant electrical function. Record the repaired location and any required cleaning or retest. A successful individual repair does not demonstrate that the production cause has been removed; the next build still needs the corrective-action trial.

How Can Our PCB Assembly Process Help Control Tombstoning?

Our PCB assembly services include DFA review, stencil fabrication, solder paste printing, 3D SPI, placement, reflow, AOI and functional testing. We support SMD packages down to 01005, with the actual assembly requirements reviewed against the component, footprint and inspection needs.

For a tombstoning investigation, these stages provide different evidence: SPI checks the printed deposit, placement review checks the chip before melting, and post-reflow inspection checks the completed attachment. Our equipment includes a SINIC-TEK S8080 3D SPI system and SINIC-TEK A510DL 3D AOI system. The equipment does not replace a project-specific process window or the agreed acceptance requirements.

Send us the PCB files, BOM with exact manufacturer part numbers, placement data and assembly drawing. For an existing defect, include clear photographs, affected reference designators, failure counts and available printing or profile records. We can then discuss the board and assembly requirements for your build. Contact sales@bestpcbs.com for PCB fabrication and assembly support.

For a tombstoning PCB problem on your build, include the affected component locations and inspection records with your assembly inquiry.

Tombstoning PCB FAQs

Can a board with a tombstoned capacitor still power on?

Yes. A disconnected decoupling capacitor may not stop startup, even though the circuit has lost part of its intended filtering. Power-on alone is not an acceptance test for the assembly.

Does lead-free solder always cause more tombstoning?

No. The actual alloy’s melting behavior, paste formulation and the joint-to-joint imbalance matter. Do not treat all lead-free alloys as one process or assume that changing alloy fixes a footprint problem.

Should every tombstone be blamed on the assembly operator?

No. Design geometry, component condition, printed paste, placement and thermal history can contribute. Preserve the evidence and identify the process contribution before assigning corrective action.

You may also like

ESP32-P4: From Development Board to Custom PCB Assembly

October 30th, 2026

ESP32-P4 gives product teams a platform for touchscreens, camera interfaces, and embedded image processing. Turning a working development-board demo into a production-ready product takes more than copying the schematic: memory selection, power delivery, connector placement, and test access all affect whether the custom board is practical to manufacture and maintain.

At EBest Circuit (Best Technology), we bring PCB fabrication, component sourcing, and assembly together so your team can move a released design into hardware with fewer supplier handoffs. Our manufacturing review focuses on details that affect the build, including component footprints, PCB stackup, soldering access, and inspection. Send your project files to sales@bestpcbs.com for a quotation based on your actual configuration.

ESP32-P4

ESP32-P4 Specifications for HMI and Camera Applications

ESP32-P4 is a strong candidate when display and camera interfaces drive the hardware architecture. Its processing and peripheral capabilities suit human-machine interfaces (HMIs), control panels, and imaging products, but the selected display, sensor, and software still determine the achievable system performance.

Specification ESP32-P4 capability
Main processor Dual-core 32-bit RISC-V, up to 400 MHz
Low-power processor Single-core RISC-V, up to 40 MHz
Display and camera interfaces MIPI DSI, MIPI CSI, and parallel interfaces
Image processing ISP, JPEG codec, and H.264 encoder
Connectivity interfaces USB 2.0 High-Speed OTG and Ethernet MAC
In-package PSRAM 16 MB on ESP32-P4NRW16X; 32 MB on ESP32-P4NRW32X
Package for these variants QFN104, 10 × 10 mm
Native wireless connectivity No integrated WiFi or Bluetooth radio

Flash capacity is a separate design choice. The PSRAM figures above describe working memory inside the specified chip packages; they do not describe nonvolatile flash. A module advertised with 16 MB or 32 MB flash must be checked against its own schematic and bill of materials.

For an HMI, size memory around frame buffers, graphics assets, and application tasks. For a camera product, also account for sensor output, buffering, and processing load. Test the intended display or sensor early, before its connector and power requirements become fixed in the enclosure.

ESP32-P4 vs ESP32-S3: Which Fits Your Product?

Choose ESP32-P4 when its multimedia interfaces and processing resources solve a specific product requirement. ESP32-S3 deserves consideration when integrated wireless connectivity and a simpler architecture meet the application’s needs.

Selection factor ESP32-P4 ESP32-S3
Main CPU Dual-core RISC-V, up to 400 MHz Dual-core Xtensa LX7, up to 240 MHz
Integrated wireless External wireless device needed 2.4 GHz WiFi and Bluetooth 5 LE
Main reason to evaluate Display, camera, and image-processing workloads Connected control and applications benefiting from integrated wireless
Board planning priority High-speed interfaces, power, and optional wireless companion Antenna layout, peripheral needs, and memory configuration

Clock speed alone is a poor purchasing criterion. Compare both devices using your actual screen resolution, refresh behavior, camera workload, and connectivity needs. A P4 design with an additional wireless device also introduces another power load, host interface, and firmware integration task; include those costs in the comparison.

ESP32-P4 WiFi: Why a Companion Chip Is Needed

ESP32-P4 has no native WiFi or Bluetooth radio. Wireless connectivity requires a companion device, such as an ESP32-C6, with its own host interface, power supply, and antenna provisions.

Make three decisions before committing to the PCB layout:

  • Choose the host interface and software together. SDIO, SPI, and UART are options in Espressif’s companion architectures, with software approaches including ESP-Hosted and ESP-AT. Match the supported combination to throughput and available pins; these are not interchangeable drop-in choices.
  • Reserve space for power and the antenna. Follow the selected module manufacturer’s carrier-board keepout rules and check clearance from display frames and metal housings. Resolving these constraints before enclosure release reduces the risk of a board or mechanical redesign.
  • Include wireless hardware only where needed. A wired-only product may not need a companion device. Removing unused circuitry reduces the BOM, assembly work, and software maintenance.

Treat the companion as part of the product architecture from the start. Adding it after the main board is routed can force changes to pin assignments, power distribution, and connector placement.

ESP32-P4 Module or Dev Board: Choosing a Starting Point

A development board is useful for evaluating peripherals and software; a module can reduce the circuitry you need to integrate on a custom carrier. A direct chip-based design gives more control over the final board’s size, connectors, and component choices.

  • Development board: Use it to validate the display, camera, software, and power behavior. Its extra connectors and debug circuitry may be unnecessary in the finished product.
  • ESP32-P4 module: Check the exact flash, PSRAM, power circuitry, exposed signals, mounting method, and wireless configuration. Module features vary by supplier and part number.
  • Custom chip-based PCB: Consider it when the enclosure or production requirements justify integrating the circuitry directly. Budget for layout review, bring-up, and a repeatable test method.

Before selecting a module, verify that it exposes every interface your product needs. A missing signal, incompatible connector, or unavailable production variant can erase the time saved during prototyping. Keep the exact module or chip ordering code in the BOM, rather than using “ESP32-P4” as a substitute for a purchasable part number.

ESP32-P4 Schematic and Pinout for a Custom PCB

Start the custom schematic with the reference design for the exact chip revision being purchased. Espressif recommends the reference schematic for revisions v3.0 and later for new designs; an older development-board schematic should not be copied without checking the differences.

One important change is pin 54: it is VDD_HP_1 in revisions v3.0 and later, whereas revisions v1.0 and v1.3 defined it as NC. A familiar-looking symbol or footprint can therefore conceal an electrical mismatch.

Review these items before releasing the board:

  • Power and reset: Check rail requirements, regulator capacity, decoupling, and startup behavior with the display, camera, and other peripherals connected.
  • Flash compatibility: Match voltage, interface mode, pin mapping, and firmware configuration to the selected flash device.
  • Boot and debug access: Protect strapping-pin states from attached circuitry and retain a practical download and recovery connection.
  • Connector mapping: Verify mating parts, cable orientation, pin numbering, and power polarity against the actual peripheral.

A pinout diagram is a starting reference, not a release checklist. The schematic symbol, PCB footprint, BOM, and assembly drawing need to describe the same device revision and connector arrangement.

PCB Stackup and Routing for MIPI, USB, and Memory

Espressif recommends at least a four-layer PCB for ESP32-P4 layouts. Plan the PCB stackup around continuous return paths and manufacturable impedance targets before routing high-speed interfaces.

Establish the layer arrangement. The suggested structure places components and signals on the top layer, a solid ground plane on layer 2, power and suitable routing on layer 3, and additional signals on the bottom. Add layers when board size or connector placement prevents clean routing; forcing a dense display-and-camera design onto two layers can create avoidable layout compromises.

ESP32-P4

Apply constraints where they matter.

  • USB and MIPI: USB guidance specifies 90 Ω differential impedance, ±10%; MIPI pairs need their own interface-specific constraints. Avoid reference-plane breaks and unnecessary transitions. Agree on trace widths and spacing with the fabricator for the actual stackup instead of copying dimensions from another board.
  • Power: Keep switching-regulator loops compact and sensitive interfaces away from noisy routing to reduce interference risks.
  • Memory: For the in-package PSRAM variants listed above, external memory routing primarily concerns the selected flash. There is no separate board-level PSRAM bus to copy from an unrelated design.

Release clear fabrication requirements. Identify impedance-controlled nets and the approved stackup in the manufacturing files. Explicit targets give the fabricator a consistent basis for building prototypes and repeat orders.

Assembling and Testing Custom ESP32-P4 Boards

A custom ESP32-P4 assembly needs control of solder deposition, component placement, and board-level test access. The QFN package and compact peripheral circuitry make those details especially important during the first build.

ESP32-P4

Our PCB assembly service includes incoming component checks, solder paste inspection, placement and reflow, AOI, and X-ray inspection where appropriate. For a P4 board, the assembly review should address the exposed-pad footprint, stencil apertures, nearby small components, and connector orientation before production starts.

Inspection and functional testing answer different questions. AOI and X-ray help assess assembly quality; they do not establish that the display, camera, or wireless software works as intended.

Build the test plan around observable results:

  • Power rails and current draw during startup and the agreed operating modes.
  • Programming, boot, and firmware version checks.
  • Display, camera, USB, and networking checks for the interfaces actually fitted.
  • Accessible test points and clear pass/fail criteria for repeat orders.

For functional testing, supply the approved firmware, test instructions, and any required fixtures or peripherals. Testing with the intended display and camera helps distinguish assembly faults from cable, driver, or configuration problems before boards reach your integration team.

From Prototype to Production: Cost and Lead Time

Custom ESP32-P4 PCBA cost depends on the complete board; lead time depends on material availability, fabrication, assembly, and testing. Comparing processor prices alone misses the choices that determine the build’s budget and schedule.

Separate setup costs from unit costs. Stencils and test fixtures are one-time charges. PCB fabrication, memory, connectivity devices, connectors, assembly, and inspection contribute to recurring costs, which also depend on order quantity and test time. Keep these categories separate when comparing prototype and production quotations so potential savings are visible.

Protect the delivery schedule and repeat-build quality.

  • Identify critical materials early. Check availability of the exact P4 variant, module, flash, connectors, and any included display or camera. Fabrication and procurement may overlap, but a missing critical part still prevents completion.
  • Plan the complete build. Include time for PCB fabrication, assembly, programming, and the agreed tests. A bare-board turnaround does not represent the delivery time for a tested PCBA.
  • Freeze the approved configuration. Carry the BOM, PCB revision, firmware image, and test criteria into repeat orders. Route substitutions through engineering review; a similar memory device or connector may still need validation.

Provide a quotation-ready file package. Send Gerber and drill files, a BOM with manufacturer part numbers, placement data, assembly drawings, quantities, and the target delivery date. Include the schematic for engineering review and describe programming and testing needs. A complete package reduces quotation follow-up and makes the price and schedule reflect the intended build.

FAQs About ESP32-P4

Are ESP32-P4 flash and PSRAM the same thing?

No. Flash retains firmware and stored data without power. PSRAM is volatile working memory. Check both capacities separately when comparing chips, modules, or development boards.

Does ESP32-P4 have native HDMI?

No. Its display interfaces include MIPI DSI and parallel options. HDMI output requires additional hardware, such as a suitable bridge, plus compatible software and a separate interface design review.

Does an ESP32-P4 Ethernet design need an external PHY?

Yes, a conventional copper Ethernet connection needs an external PHY and the appropriate connector, magnetics, and protection circuitry. The integrated Ethernet MAC does not provide the complete physical interface.

Does an ESP32-P4 PCB require high-frequency laminate?

Not automatically. Select the laminate and stackup around trace lengths, signal rates, loss, impedance, and thermal requirements. FR4 may be suitable; a high-speed interface alone is not a reason to specify a specialty laminate.

Can EBest Circuit assemble boards using customer-supplied components?

Yes. We provide consignment, partial turnkey, and full turnkey assembly. Identify supplied parts in the BOM and agree on packaging, quantities, and handling before the build.

Bring your custom ESP32-P4 board to EBest Circuit (Best Technology) for coordinated PCB fabrication, component sourcing, and PCBA assembly. Our DFM support connects stackup and footprint decisions with assembly inspection and functional testing based on your approved firmware and test plan, helping address build risks before production. 1.5-week PCBA quick delivery is available for eligible projects, with material availability, board complexity, and testing needs reviewed before the schedule is agreed. Send your project files, quantities, and target delivery date to sales@bestpcbs.com for a quotation and a build plan matched to your design.

You may also like

Turnkey Box Build Assembly & Testing Contract Manufacturer

October 29th, 2026

OEMs searching for “Contract manufacturers turnkey box build assembly testing” can work with EBest Circuit for turnkey box build assembly and testing, including PCB fabrication, component procurement, PCBA and final integration managed within one project. We coordinate the board, wiring, enclosure and agreed testing to reduce manufacturing handoffs for your team.

Our support combines SMT and through-hole assembly with DFM review, tooling assessment and firmware loading. Our quality-system credentials include ISO 9001:2015, ISO 13485:2016, IATF 16949 and AS9100D, supporting OEM supplier qualification with project-specific review of the applicable site and certification scope. Send your requirements to sales@bestpcbs.com to discuss the manufacturing route and quotation for a wired subassembly or enclosed unit.

Contract manufacturers turnkey box build assembly testing
Illustrative box build integrating a PCBA, wiring and enclosure.

Turnkey Box Build Assembly Services from an OEM Contract Manufacturer

Our turnkey box build assembly service is configured around the product you need to receive. You can retain selected suppliers while assigning electronics manufacturing, mechanical integration and testing to one project.

Service area Work available Scope to define
PCB and PCBA Fabrication; SMT and through-hole assembly Board and assembly specifications
Component sourcing Procurement against the approved BOM Supplied parts and approved alternatives
Wiring and enclosure integration Cable connections and mechanical fitting Harness drawings and housing layout
Firmware loading Load the released software image Programming method and configuration
Functional testing Agreed electrical and functional checks Coverage, fixtures and acceptance limits
Packaging Product protection and shipment preparation Labels, accessories and packing requirements

Components are sourced from manufacturers or authorized distributors. Proposed substitutions require approval before entering the released configuration.

  • Full Turnkey — We procure the agreed electronic and mechanical items and coordinate assembly.
  • Partial Turnkey — You retain selected sources, such as a housing supplier or proprietary module; we source the remainder and integrate the supplied parts.
  • Consignment — You supply the agreed materials; we perform the contracted assembly and verification.

For a customer-supplied housing, our engineering review connects its drawing with PCB mounting points, connector positions and cable exits. A connector change therefore receives both a pinout and fit review before it creates a problem at final assembly.

Contract Manufacturing Solutions for Industrial, Medical and Other OEM Products

We match the manufacturing work to the product’s assembly sequence and delivery requirements, so electronics, wiring and verification are prepared for the same configuration.

Product application Manufacturing need EBest support Customer value
Industrial controller Accessible terminals and mounting screws Mixed assembly and harness integration Fewer access problems during installation
Communications unit Programming before enclosure closure Firmware loading and external-interface checks Verification in the delivered configuration
Medical electronic subassembly Controlled parts and handling Released-BOM assembly, cleaning and specified tests Alignment with OEM manufacturing requirements
Enclosed power interface Board clearance and wired power Lead trimming, fitting and electrical checks Electronics prepared for housing integration

For industrial equipment, wire harness integration is reviewed alongside fastening access and cable routing. For communications units, we assess protocol software, connected equipment and expected responses before defining the production test.

Medical projects also require review of the manufacturing site and applicable certification scope. Electronic assembly capability does not establish approval for every finished medical device.

Turnkey Box Build Assembly Lead Time and Production Planning

Our order review connects process, programming and tooling requirements with material readiness. Pre-production coordination adds special assembly and packaging needs before the schedule is released.

Preparation stage Work coordinated Release dependency
Engineering review BOM and assembly feasibility checks Resolved questions and matching revisions
Procurement Electronic and mechanical purchasing Approved parts and supplier availability
Assembly preparation Programs, instructions and fixture planning Stable mounting and interface dimensions
Test preparation Procedures, software and equipment Released firmware and acceptance limits
  • Parallel preparation — Approved purchasing can run alongside assembly-program and instruction preparation. Fixture completion depends on stable connector and mounting positions.
  • Customer changes — Review purchased stock, work in progress, fixture compatibility and test updates; define the change’s cut-in point and issue instructions to affected operations.

The schedule separates production completion, dispatch after release and packing, and transport to your site. Repeat orders may reuse tooling and programs, while material availability and revision work determine the quoted lead time.

Box Build Assembly Testing and Quality Control

Our equipment includes SINIC-TEK S8080 3D SPI, SINIC-TEK A510DL 3D AOI and UNICOMP AX8200 X-ray. Inspection identifies paste, placement and solder-joint issues while the board remains accessible, before enclosure integration.

Verification stage Main coverage Does not replace
Incoming inspection Part identity and visible condition Complete product function testing
AOI inspection Placement and visible solder defects Hidden-joint or system testing
X-ray inspection Selected hidden solder-joint features Electrical operation under load
Board functional test Defined PCBA functions and interfaces Testing installed wiring and enclosure
Integrated system test Specified assembled-product operating functions Every environmental or lifetime test

A board that works on the bench can still have a reversed cable or incorrect configuration after installation. We assess final verification against the customer’s specification.

  • Power and outputs — Apply specified supply and load conditions; measure at the designated output or final connector.
  • I/O and communications — Exercise required channels and compare responses with approved limits.
  • Firmware and configuration — Verify the released software identity and settings.
  • Installed connections — Check connector engagement, routing and specified assembled functions.

The customer specification sets operating conditions, pass/fail limits and required records. Custom fixtures, protocol programs, burn-in, environmental and electrical safety tests receive separate equipment, development and duration assessments before inclusion in the quotation.

Contract manufacturers turnkey box build assembly testing
Board inspection and integrated-product testing address different verification needs.

Contract Manufacturing Quality Systems, Certifications and Traceability

EBest uses MES-supported production management and ERP–MES data synchronization to support order follow-up. Our quality approach separates production execution, the records required for each project, and supplier certification review.

Production control What we manage OEM benefit
Engineering order review Process, programming and tooling requirements Issues addressed before production
First-article confirmation Initial setup and assembly checks Early review of manufacturing configuration
Trial-production follow-up Issue analysis and corrective actions Improvements carried into subsequent builds
MES and ERP coordination Production and material information Support for order follow-up
Process-document maintenance Assembly programs and SOP updates Consistent instructions for repeat orders

Our engineering team has resolved repeat-order program issues and incorporated the handling into SOPs, making the correction available to subsequent builds.

  • Project traceability — The agreed package may include material lots, BOM/PCBA revisions, firmware configuration and inspection or test results. Serial-number linkage, individual reports and retention periods are specified for the order; MES use alone does not establish that coverage.
  • Certification — For requirements involving ISO 9001, ISO 13485, IATF 16949 or AS9100D, we review current applicable documentation against the manufacturing entity, site and activities. Quality-system certification does not replace finished-product approval.

Box Build Assembly Case Study: Integration, Testing and Results

An enclosed 5 V power interface assembly connects a wired input to a board-mounted output connector inside a customer-supplied black housing. The customer retained the housing source while assigning electronic procurement and PCBA assembly to EBest, with defined electrical and mechanical checks.

PCB specification Project requirement
Layer count 2 layers
Base material FR4
Finished board thickness 1.6 mm ±10%
Copper thickness 1 oz on each side
Surface finish Lead-free HASL
Solder mask / legend Green / white

Protruding through-hole leads could interfere with the housing below the board. The revised instructions explicitly require even lead trimming and link the PCB/PCBA versions, keeping the fit correction aligned with the changed drawings and BOM.

Integration requirement Manufacturing response Verification method
Revised electronic configuration Match PCB, PCBA and BOM versions Review released files and component requirements
Board-to-housing clearance Trim protruding through-hole leads evenly Install board and tighten housing screws
Cable-to-connector power path Define the input/output voltage check Apply 5 V; check connector output

The engineering outcome is a documented fit correction with complementary electrical and mechanical checks. Keeping that instruction with the released revision gives repeat orders a clear assembly basis, while the OEM retains its housing supplier. Output tolerance and load conditions belong in the approved electrical procedure; sealing performance requires a separate test.

Contract manufacturers turnkey box build assembly testing
Conceptual lead-clearance comparison; not to scale.

Why Choose EBest Circuit as Your Box Build Contract Manufacturer

EBest Circuit connects board manufacturing with the engineering and production controls needed for an integrated OEM build.

  • PCB/PCBA manufacturing foundation — Our PCB assembly services cover fabrication, SMT and through-hole assembly, supported by Yamaha YSM20R placement equipment and board inspection. Integration issues can be investigated alongside their placement or soldering process, reducing separate supplier handoffs.
  • DFM engineering support — We review BOM ambiguities, footprint mismatches, assembly access and tooling requirements. The OEM receives specific manufacturing questions to resolve before they become production interruptions.
  • Flexible sourcing — Full turnkey, partial turnkey and consignment arrangements allow qualified housing suppliers or proprietary components to remain in the project. We coordinate the remaining contracted work around those supplied items.
  • Prototype-to-repeat production continuity — Our electronics NPI services connect manufacturing review with trial-build preparation. Approved corrections move into instructions or programs, preserving first-build learning for later orders.
  • Quality records matched to the order — MES-supported management, first-article confirmation and maintained SOPs support manufacturing follow-up. Project-specific traceability and test records are agreed with the OEM to support change review and supplier assessment.
  • Certification support for OEM qualification — Our ISO 9001:2015, ISO 13485:2016, IATF 16949 and AS9100D credentials provide a basis for reviewing quality-management requirements during supplier approval. We match the applicable certificate, manufacturing site and scope to your project, helping your team assess supplier suitability without treating company certification as finished-product approval.

Turnkey Box Build Assembly Cost, Testing Scope and Quotation

We assess assembly work, tooling and test preparation with the project so the quotation separates per-unit manufacturing from one-time engineering charges. Test coverage remains explicit: identical BOMs do not necessarily mean identical deliverables.

Cost element Main pricing inputs Typical cost treatment
PCB and components Board specification, BOM and availability Recurring material and manufacturing cost
PCBA processing Placement, soldering and inspection Setup plus recurring processing
Harnesses and enclosures Drawings, connectors, finish and quantities Parts plus applicable tooling
Final assembly Fastening, routing and configuration Recurring assembly labor
Functional testing Coverage, cycle time and operator involvement Recurring test execution
Fixtures and test development Interfaces, equipment and software Separate engineering or tooling charge
Packaging and delivery Protection, labeling and shipment terms Order-specific packing and freight

For comparable quotations, specify three items.

  1. Supply arrangement — Full turnkey, partial turnkey or consignment, including responsibility for housings and cables.
  2. Delivery and acceptance — PCBA, wired subassembly or enclosed unit, with firmware, test coverage and required records.
  3. Quantity and tooling — Order quantities, target dates and available fixtures. Connector or firmware changes may require fixture or program updates on repeat orders.

Send your BOM, Gerber files, assembly drawings, quantities, target delivery date and test requirements to sales@bestpcbs.com. Enclosure CAD and harness drawings help us assess the remaining integration work.
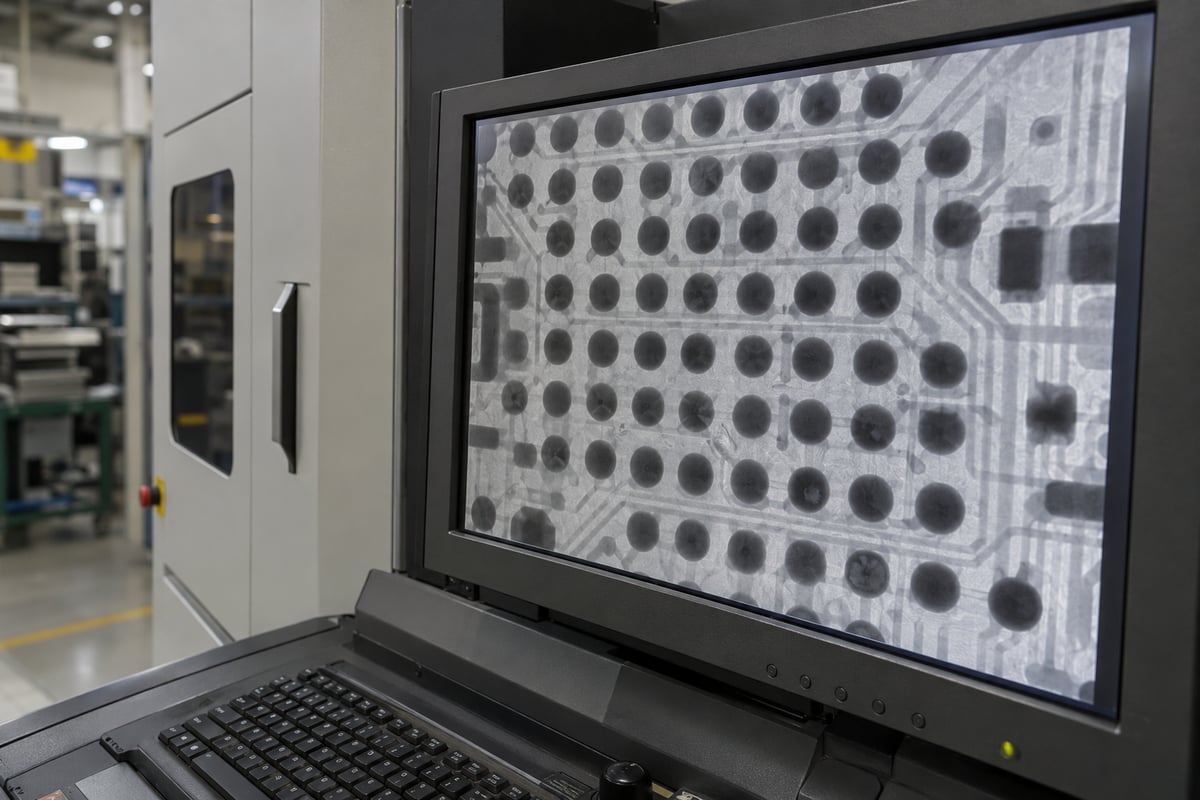
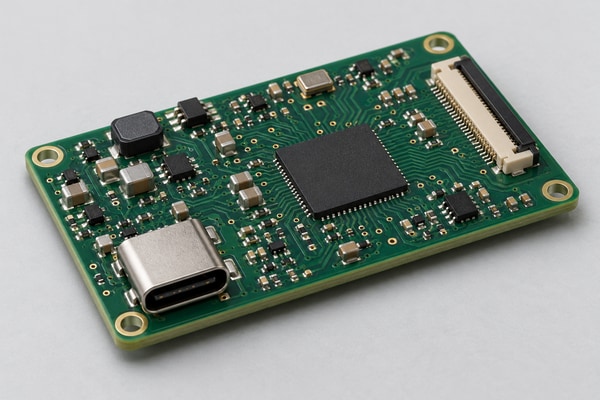
FAQs About Contract Manufacturing, Box Build Assembly and Testing

Can we supply our own PCBAs or components?

Yes. We offer consignment and partial-turnkey arrangements. Identify supplied items, quantities, revisions and arrival dates so receiving and assembly can be scheduled together.

What information is needed if our manufacturing files are incomplete?

Start with the available BOM, board files, drawings and required functions. Samples or photographs help explain the assembly; controlled dimensions, pin assignments and acceptance limits still need to be resolved before the relevant work is released.

Does firmware loading include firmware development?

No. Loading uses an approved image, revision and programming method. Firmware development, debugging or test-software creation requires a separately agreed scope.

How are test fixtures and test programs handled?

You may supply an existing setup, or the project may require development. The quotation identifies that work, maintenance responsibility and fixture ownership or transfer arrangements.

Are burn-in and other special tests included automatically?

No. We assess the specified conditions, duration and acceptance criteria for equipment suitability, then include the agreed testing in the quotation.

When can a firm production lead time be confirmed?

After reviewing scope, revisions, material availability, tooling and testing. The schedule separates production completion, dispatch preparation and transit, with outstanding approvals identified.

How are component and firmware changes handled for repeat orders?

We review their effect on fit, electrical behavior, assembly instructions and testing against the released revision. A firmware change may require a new test-program version even if the hardware is unchanged.

Send your BOM, Gerber files, assembly drawings, quantity, target delivery date and test requirements to sales@bestpcbs.com for enquiries about Contract manufacturers turnkey box build assembly testing. We can assess the work you want to transfer and prepare a quotation for the required delivery state.

You may also like

Turnkey PCBA Supplier in Vietnam for OEM Electronics

October 29th, 2026

A PCBA supplier in Vietnam should connect local assembly with dependable component sourcing, engineering support and product testing. EBest Circuit (Best Technology) provides Vietnam PCBA manufacturing supported by its wider PCB and electronics manufacturing network, helping OEM teams move from a circuit design to assembled boards and integrated products.

Founded in 2006, EBest Circuit combines Vietnam assembly with PCB manufacturing, component sourcing and engineering resources in China. OEM teams can address board manufacturability, material availability and assembly requirements through one partner, reducing handoffs between separate suppliers. Our DFM support helps resolve production issues before the build, whether you are introducing a new product or qualifying a second source. Contact sales@bestpcbs.com to discuss your project and quotation requirements.

PCBA supplier in Vietnam

PCBA Services Offered by EBest Circuit

EBest Circuit supports prototype, low-volume and repeat-production PCBA projects. Customers can work with us for PCB assembly services alone or combine bare-board supply, components, assembly and testing in a turnkey order.

Service Scope
PCB supply FR4, metal-core, ceramic, flex and rigid-flex boards
Component sourcing BOM procurement and alternative-part review
PCB assembly SMT, THT, double-sided and mixed assembly
Engineering support DFM, DFA, BOM review and programming support
Inspection and testing SPI, AOI, X-ray and project-specific electrical tests
Product integration Wire harnesses, enclosure assembly and final testing

The manufacturing route depends on the substrate, component mix and finished-product requirements. For example, a compact controller may combine fine-pitch ICs with through-hole connectors, while a metal-core lighting board requires soldering conditions suited to its thermal behavior. Our engineering team connects these requirements with the assembly process before production.

PCBA Factory in Vietnam: Production Location and Project Support

EBest Circuit’s PCBA factory in Bac Ninh, Vietnam, provides local assembly supported by PCB manufacturing, component sourcing and engineering resources in China. This arrangement gives OEM teams a Vietnam production option while coordinating board supply, assembly and delivery through one manufacturing partner.

  • Vietnam PCBA Manufacturing — Our Vietnam factory supports SMT, through-hole and mixed assembly, connecting solder paste printing, component placement, reflow, leaded-component soldering and inspection within the agreed production route.
  • Production Equipment — Manufacturing resources supporting our projects include Yamaha YSM20R placement, nitrogen reflow, 3D SPI and X-ray inspection. Equipment and inspection coverage are matched to the assigned factory and assembly requirements, including fine-pitch components and hidden solder joints.
  • China–Vietnam Manufacturing Support — China-based PCB fabrication, component procurement and engineering resources support Vietnam assembly. Coordinating these activities helps align board specifications, BOM availability and material arrivals with the production schedule.
  • Engineering & Project Support — Our team reviews design files, BOM details and assembly requirements, then coordinates engineering questions and revision changes before they reach production. Customers have a defined point of contact for both technical and commercial issues.
  • Production Visibility & Delivery Coordination — Order updates connect material readiness, production progress and quality records with shipment planning. Digital traceability supports investigation of material and batch history when engineering or purchasing teams need project information.

SMT, Through-Hole and Mixed PCB Assembly Capabilities

EBest Circuit assembles small surface-mount devices, fine-pitch packages and through-hole components, including boards that combine all three. Our capability includes 01005 SMD components and BGA pitch down to 0.25 mm, subject to the board layout, package requirements and process review.

Manufacturing Parameter Specification
Minimum SMD size 01005
Minimum BGA pitch 0.25 mm
Assembly configuration Single-sided, double-sided and mixed assembly
Package support BGA, QFN, QFP and discrete components
Component presentation Reels, cut tape, tubes and trays
Reflow process Nitrogen reflow available
Through-hole processes Wave soldering and manual soldering
Additional assembly Wire harness and connector assembly
Engineering services DFM, DFA, BOM verification and IC programming

Minimum component size and pitch are process capabilities, not automatic approval of every layout. Pad geometry, stencil design, component clearance, board support and thermal behavior determine the production setup.

SMT assembly supports compact circuitry and dense placement. Solder paste inspection precedes component placement, while reflow conditions are matched to the assembly rather than treated as a single profile for every board.

Through-hole and mixed assembly support connectors, transformers, relays and other leaded components alongside SMT circuitry. The assembly sequence accounts for component temperature limits and access to solder joints, reducing unnecessary handling between operations.

PCBA supplier in Vietnam

Turnkey vs. Consigned PCBA: Component Sourcing Options

EBest Circuit offers full turnkey PCB assembly, partial turnkey and consigned assembly. The difference is mainly who purchases and supplies the components; the required assembly quality remains tied to the same product specifications.

Supply Model Component Supply Typical Fit
Full turnkey EBest Circuit procures the BOM Consolidated purchasing and assembly
Partial turnkey Customer and EBest Circuit share supply Customer-controlled ICs or selected inventory
Consigned assembly Customer supplies the component kit Existing stock or established procurement contracts

Our purchasing team sources components directly from manufacturers or authorized distributors, including DigiKey, Mouser, Future Electronics, TTI, Avnet and Arrow. BOM review addresses manufacturer part numbers, packages and availability before components reach the assembly line.

When a specified part is unavailable, engineering can propose alternatives for customer approval. Matching a package alone is insufficient: electrical ratings, pin assignments and operating requirements also matter.

Partial turnkey is particularly useful when an OEM already holds a critical processor or custom connector but wants EBest Circuit to procure the remaining BOM. Consigned projects also need suitable packaging and sufficient quantities for feeder loading and production losses.

DFM and NPI Support from Prototype to Production

EBest Circuit’s DFM and DFA support connects board design with the practical requirements of placement, soldering and inspection. During new product introduction, the focus is on resolving manufacturing issues before they repeat across a larger batch.

  • Pad and stencil design — Review solderable areas and paste openings for fine-pitch and bottom-terminated packages.
  • Placement access — Review component spacing, polarity information and access around tall parts.
  • Panel and board support — Assess fiducials, tooling features and handling requirements, particularly for thin or irregular boards.
  • BOM and assembly data — Reconcile part numbers, footprints, placement data and assembly drawings.
  • Test access — Consider programming connections and accessible test points alongside the planned test method.

For a mixed-technology controller, this may mean addressing a connector’s soldering access while refining paste deposition around a nearby QFN. For a double-sided assembly, component placement and the soldering sequence need to work together.

Prototype findings can then inform the next build’s assembly instructions, component choices and inspection requirements. This gives the transition to repeat production a technical basis beyond simply increasing the order quantity.

PCBA Inspection, Functional Testing and Quality Records

EBest Circuit uses incoming checks, in-process inspection and product testing to control different failure risks before shipment. The quality plan connects the approved BOM and assembly requirements with inspection coverage, acceptance limits and the records required for the order.

Equipment / Control Production Risk Addressed Order-Specific Documentation
Incoming inspection and BOM verification Incorrect parts or unsuitable incoming material Incoming inspection results; agreed material identification
SINIC-TEK S8080 3D SPI Abnormal paste deposits before placement Agreed SPI results and exception records
SINIC-TEK A510DL 3D AOI Placement errors and visible solder defects Inspection results; repair and reinspection records
UNICOMP AX8200 X-ray Hidden-joint bridging and unacceptable voiding Images and findings for agreed inspection coverage
ICT and functional testing Circuit faults and failed operating functions Test revision, limits and pass/fail results
Aging testing, when specified Failures under defined duration and load Conditions, duration and recorded results
Final inspection and release Incomplete builds or identification errors Final inspection and agreed release documentation

Equipment names identify EBest Circuit manufacturing resources, not an identical equipment list at every facility. For Vietnam PCB assembly orders, the assigned site, available record exports, traceability depth and retention requirements must be agreed before production. The documentation column defines items to specify in the quality plan; it is not a standard report package included with every order.

SPI findings allow printing issues to be reviewed before components are placed. AOI or X-ray findings guide defect review, repair where permitted and reinspection. Functional testing then checks the specified operating behavior—acceptable-looking solder joints alone do not establish that a board works correctly.

For projects requiring production history, define how board or lot identifiers connect to material, inspection, test and rework records. Our SMT traceability log guide explains the difference between lot-level and unit-level records, helping OEM teams specify useful evidence rather than an undefined “full traceability” requirement.

Box Build Assembly and Finished Product Integration

EBest Circuit can combine PCBA, wire harnesses, enclosure assembly and agreed product-level testing to deliver a complete module or finished unit. This extends Vietnam assembly projects beyond populated boards to the electrical and mechanical interfaces needed for the final product.

  • PCB installation — Fit assembled boards to the specified mounting points, supports and enclosure layout.
  • Harness and connector integration — Incorporate custom wire harnesses and internal connections to the approved wiring requirements.
  • Enclosures and mechanical parts — Coordinate metal or plastic housings with sheet-metal, CNC-machined or injection-molded parts as required.
  • Product-level testing — Test the integrated assembly against agreed power, interface and operating requirements.
  • Final delivery scope — Supply assembled modules or finished units with the specified identification, packaging and test documentation.

For example, in a controller housed in an enclosure, board placement, connector access and harness routing must work together. Reviewing those interfaces alongside PCBA avoids leaving fit problems to a separate final assembler.

With one project covering the board, wiring and housing, OEM teams have fewer supplier interfaces to coordinate. The delivered item can be a tested integrated assembly, ready for the customer’s next installation or acceptance step, rather than separate electrical and mechanical parts.

PCBA supplier in Vietnam

PCBA Cost, Lead Time and Delivery Planning

EBest Circuit plans PCBA quotations around the actual material and production route, including component readiness, assembly setup and test development. For PCB assembly in Vietnam, an achievable delivery date also depends on when boards, components and any mechanical parts reach the assigned facility.

Quotation Condition EBest Circuit Support Information Needed
Long-lead or unavailable components Review availability and propose approved alternatives Exact part numbers; substitution restrictions
Customer-held critical components Use partial turnkey or consigned supply Available quantities, packaging and arrival dates
PCB features adding fabrication cost Review manufacturability and permitted design changes Stackup, materials, tolerances and design constraints
Repeat-build tooling Assess existing stencil and fixture compatibility Design revision and available tooling
Small batches with high setup cost Compare feasible quantities and material purchasing options Prototype quantity and expected follow-on demand
Custom functional testing Plan fixture development and test scope before scheduling Firmware, interfaces, loads and pass/fail limits
Box build or Vietnam delivery requirements Coordinate mechanical parts, assembly and shipment sequence Drawings, production location and destination

Reusing compatible tooling can avoid unnecessary engineering charges, but a layout or test-interface change may require modification or replacement. Similarly, an approved component alternative may resolve a sourcing delay, while an unapproved substitution simply transfers risk into production.

A useful supplier comparison separates one-time tooling and engineering from recurring unit costs, and identifies which tests, mechanical parts and freight are included. EBest Circuit can review the build on that basis so price differences reflect the same scope.

Lead time begins with material and engineering readiness. A board awaiting a long-lead IC cannot complete assembly simply because SMT capacity is available. Production planning therefore connects sourcing, board supply, assembly, testing and shipment rather than presenting one unconditional turnaround figure.

Why Choose EBest Circuit as Your PCBA Supplier in Vietnam?

EBest Circuit combines certified Vietnam manufacturing with experienced PCB/PCBA engineers, its own manufacturing resources and a coordinated supply chain. For OEM customers, that means support for both the assembly itself and the engineering, sourcing and delivery work behind it.

  • Certified Manufacturing Quality — Our Vietnam factory holds ISO 9001, ISO 13485, IATF 16949 and AS9100D certifications. These quality systems support supplier audits and the quality-management expectations of medical, automotive and aerospace customers.
  • Dedicated 1+3 Technical Support — One sales representative works with three engineering and technical specialists to support your project from initial review through production and delivery. This connects commercial communication with direct responses to design and process questions.
  • DFM Support from Engineers with 20 Years of Experience — Our R&D and PCB/PCBA engineers provide DFM pre-review reports and BOM optimization lists. Manufacturability analysis, process recommendations and design support help resolve production concerns before the build.
  • Own Manufacturing Resources and 1,000+ Supply-Chain Partners — Across our China–Vietnam operations, we combine PCB manufacturing, component sourcing, PCBA, inspection and testing, with product integration where required. Our supplier network supports component procurement and production coordination while reducing the number of separate suppliers an OEM needs to manage.
  • Prototype-to-Volume Support and Fast Turnaround — We support prototypes, small batches and follow-on volume production. Eligible PCBA projects can achieve approximately 1.5-week turnaround, subject to material readiness, process requirements and the agreed project scope.
  • Digital Production Traceability — Our digital workshop supports retrieval of material, product-batch and related production records and progress information within 5 seconds. This gives project teams faster access to the information needed for status reviews and quality investigations.
  • 20 Years of PCB/PCBA Manufacturing Experience — EBest Circuit has served 10,000+ engineers and 1,800+ customers. This experience supports design review, prototype validation and the transition to repeat production within one manufacturing relationship.

FAQs About Working with a PCBA Supplier in Vietnam

Can EBest Circuit help if my design is not ready for manufacture?

Yes. PCB design and engineering support are available. An incomplete design starts with development and review work; a firm production quotation depends on sufficiently defined board, component and assembly requirements.

Can obsolete components be replaced during a PCBA project?

Engineering can review candidate replacements, but alternatives require customer approval. A replacement may affect the footprint, circuit behavior or firmware, so an obsolete part is not always a direct substitution.

Does a repeat order need another prototype?

Not necessarily. An unchanged, established design may proceed to a repeat build. Changes to components, board layout, firmware or manufacturing conditions can justify first-article checks or further validation.

Can IC programming be included?

Yes. IC programming support can be included in the assembly scope. The build requires the correct firmware version, programming method and verification requirements.

Can a test sample replace a written functional test specification?

A reference sample can help define expected behavior, but it does not describe every operating limit. Functional testing also needs defined inputs, outputs, loading conditions and pass/fail criteria.

Can EBest Circuit be evaluated as a second PCBA supplier?

Yes. A qualification build can be discussed using the approved design revision, BOM, firmware and acceptance tests. Existing stencil and fixture compatibility should be assessed rather than assumed, and qualification results should be reviewed before repeat production.

Looking for a PCBA supplier in Vietnam for a new product or second-source program? As an experienced PCBA manufacturer in Vietnam, EBest Circuit combines manufacturing experience since 2006 with Vietnam assembly and China-based PCB, sourcing and engineering support, helping your team coordinate the build through one partner. Send your Gerber files, BOM, quantities and project requirements to sales@bestpcbs.com for a quotation, including any required Vietnam production, testing or box build scope.

You may also like