PCB manufacturing PCB manufacturing
Home > Blog

Data Center Server Refresh Cycle: PCB Demand in 2026

November 6th, 2026

The data center server refresh cycle pcb demand 2026 outlook depends on three things: when operators replace equipment, how many new systems they deploy, and how much PCB content each system contains. A refresh creates new board demand when it requires new hardware, but consolidation can reduce server counts while increasing manufacturing complexity per board. In 2026, AI-related spending adds another driver alongside ordinary replacement. For PCB buyers, the useful question is not simply how old a server is; it is which motherboard, accelerator, networking, storage, and power designs are being released for production.
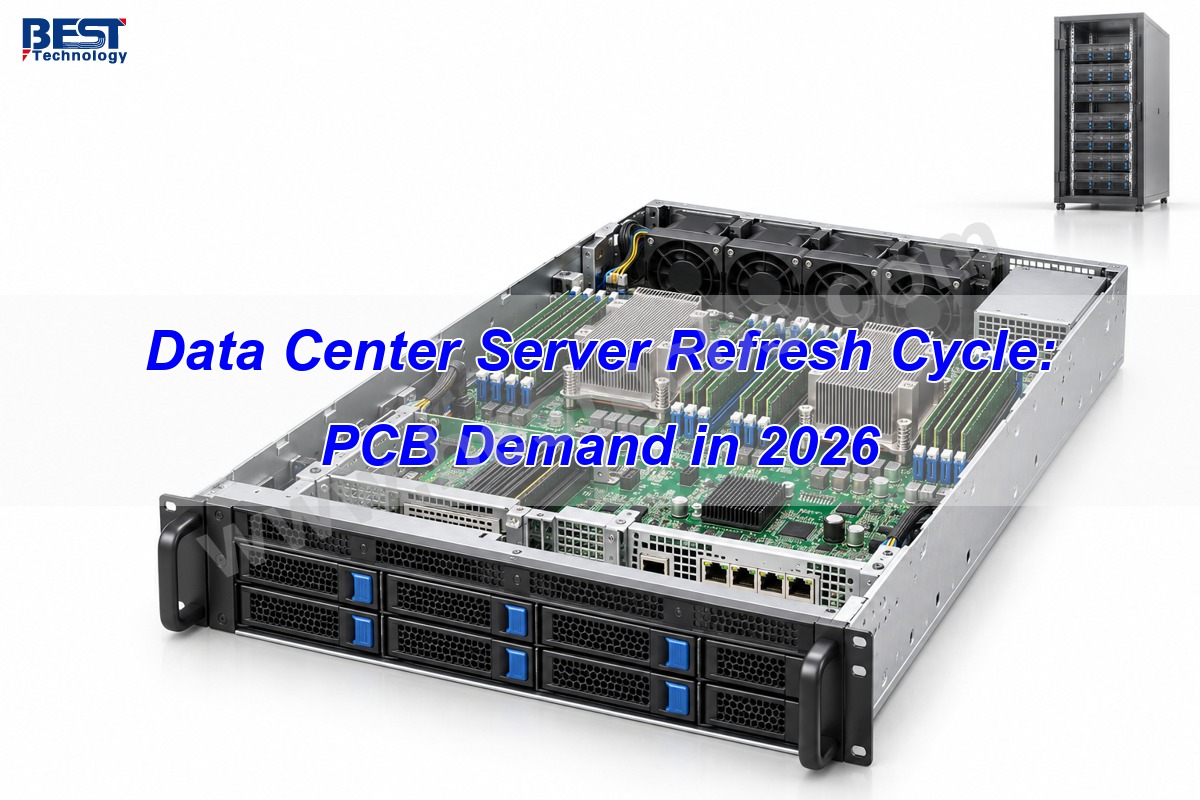
Data center server refresh cycle hardware: open rack server tray with motherboard and memory slots

Key Takeaways

  • A refresh cycle is a planning decision, not an automatic retirement date or an accounting depreciation period.
  • PCB demand comes from replacement systems, new capacity, supporting network and power equipment, and service spares.
  • TTM reported that Data Center and Networking represented 41% of its third-quarter 2026 net sales; that is a supplier sales mix, not global PCB market share.
  • AI hardware can change laminate selection, routing density, power distribution, and assembly inspection requirements without imposing one universal layer count.
  • Server consolidation can reduce board units even when each replacement system contains more expensive electronics.
  • For manufacturing, approved stackups, controlled material substitutions, inspection coverage, and release schedules matter more than a headline market growth rate.

How Long Is a Data Center Server Refresh Cycle?

A data center refresh cycle is workload-dependent: a three-to-five-year replacement window can be a starting planning scenario, but it is not a rule for every fleet or every server component.

Operators replace equipment when performance, operating cost, support coverage, security requirements, or failure exposure justify the change. An underused server may remain useful after a newer generation arrives. A heavily loaded platform may become uneconomic sooner because it consumes too much power or rack space for the work it delivers.

Accounting life measures something different. Microsoft’s fiscal 2026 annual report lists estimated useful lives of two to six years for servers and network equipment. That range describes depreciation assumptions; it does not mean every Microsoft server is physically replaced at either endpoint. A data center replacement cycle should therefore be evaluated against the actual workload and support plan, not copied from an annual-report accounting policy.

At EBest Circuit, we support the manufacturing side of hardware changes through PCB fabrication, DFM review, component sourcing, and PCB assembly services. Our starting point is the released board design and its acceptance requirements—not an assumed replacement age.

Data Center Server Refresh Cycle: What Does the 2026 Evidence Show?

Public 2026 disclosures show strong data-center-related activity, but they do not establish a single global PCB growth rate caused by server refreshes.

Source and period Reported evidence Demand signal
TTM, results released October 22, 2026; quarter ended September 28 Data Center and Networking accounted for 41% of total net sales; TTM attributed strength to continued AI demand. Observed exposure to an active electronics end market.
Dell Technologies, fiscal 2026 annual report filed March 16, 2026 Modernization and consolidation contributed to demand and revenue growth in traditional servers and networking. Replacement can accompany consolidation, not just fleet expansion.
Microsoft, fiscal 2026 annual report Servers and network equipment have estimated accounting useful lives of two to six years. Asset-life assumptions vary; they are not direct PCB purchase forecasts.

These sources describe different things: supplier sales, server-market conditions, and accounting policy. Combining them into a precise PCB shipment forecast would require additional data on system shipments, board content, prices, inventory, and customer production schedules.

For planning as of November 6, 2026, our conclusion is narrower: refresh programs and AI infrastructure are both relevant demand drivers, while the timing and value of a specific PCB order remain design- and program-dependent. This is a manufacturing interpretation of the disclosures, not a full-year market forecast.

How Do Refresh, Expansion, and Redeployment Differ?

Refresh replaces installed equipment, expansion adds capacity, and redeployment moves existing equipment to another use; only the first two necessarily involve newly manufactured systems.
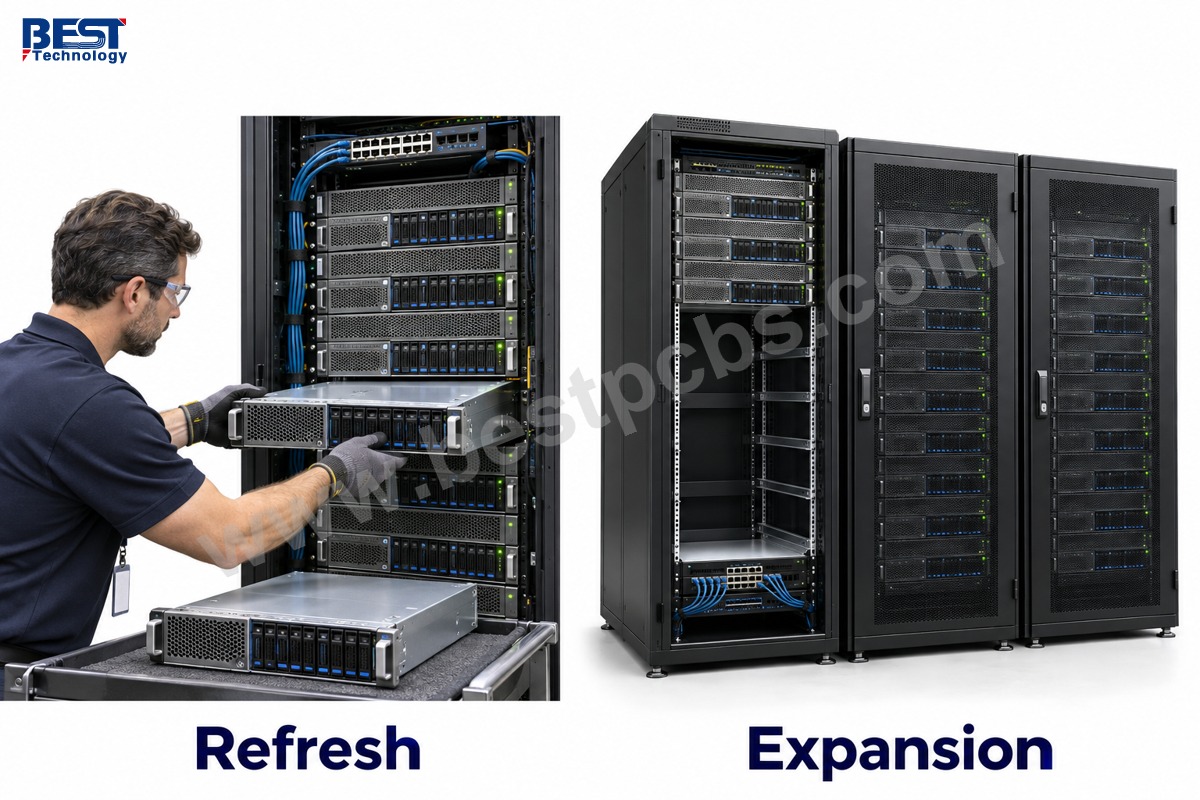
Data center server refresh cycle compared with adding new rack capacity
  • Refresh: replacing an older compute platform can require a new motherboard, memory interface, risers, and compatible power hardware.
  • Expansion: additional servers can also require more switches, storage connections, management electronics, and power distribution.
  • Redeployment: moving a retired production server into a development environment reuses its existing boards unless repair or modification is needed.

A program can contain all three. Counting the same server first as a replacement and again as an expansion unit overstates demand. Procurement plans should separate newly built systems from reused hardware before estimating board quantities.

Which PCBs Change During a Server Refresh?

Motherboards, accelerator carriers, network adapters, storage backplanes, and power-control boards can change, depending on which interfaces and mechanical assemblies the new platform retains.
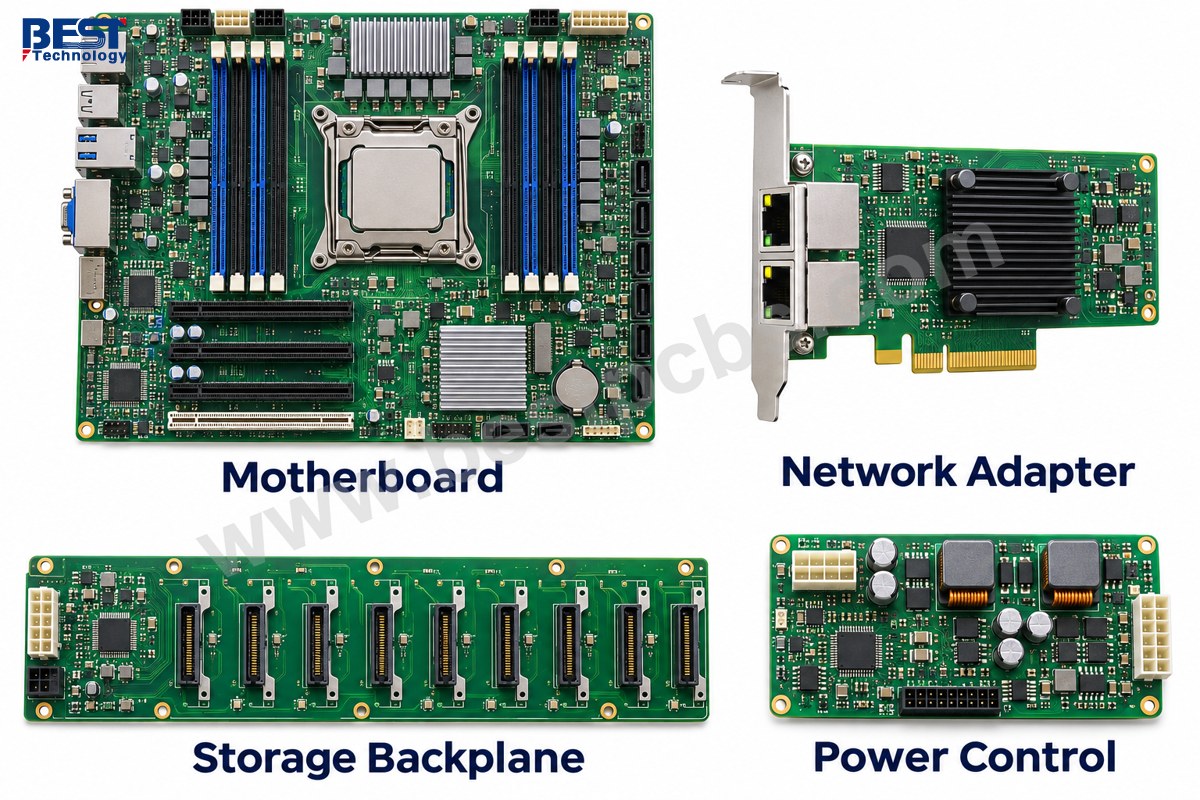
Server motherboard, network adapter, storage backplane and power control PCB examples
Board type Function Typical redesign trigger
Server motherboard Connects processors, memory, management and system interfaces Processor socket, memory generation, power architecture
Accelerator carrier or baseboard Connects accelerator modules, host interfaces and power Module footprint, interconnect topology, current demand
Network adapter or switch PCB Moves data within and between systems Link speed, port density, connector changes
Storage backplane Connects drive bays to data and power interfaces Drive interface, connector geometry, hot-swap arrangement
Power-control or distribution PCB Distributes, regulates or monitors electrical power Load current, protection, connector and cooling changes

Not every board changes in every refresh. A compatible storage backplane may remain in service while the compute board is replaced. Conversely, a new accelerator platform can force changes in the carrier, power connections, and cooling arrangement together. A data center PCB bill of materials should identify these retained and redesigned assemblies separately.

How Does AI Hardware Change PCB Requirements?

AI hardware changes PCB requirements when its interfaces, package density, power demand, or cooling arrangement exceed the existing board design’s margins.

Higher-speed channels require control of dielectric loss, copper roughness, via stubs, connectors, and reference-plane continuity. More routing layers can help distribute signals and power, but adding layers does not automatically solve channel loss. Our PCB design guidance supports the early discussion of stackup and manufacturability before fabrication data is frozen.
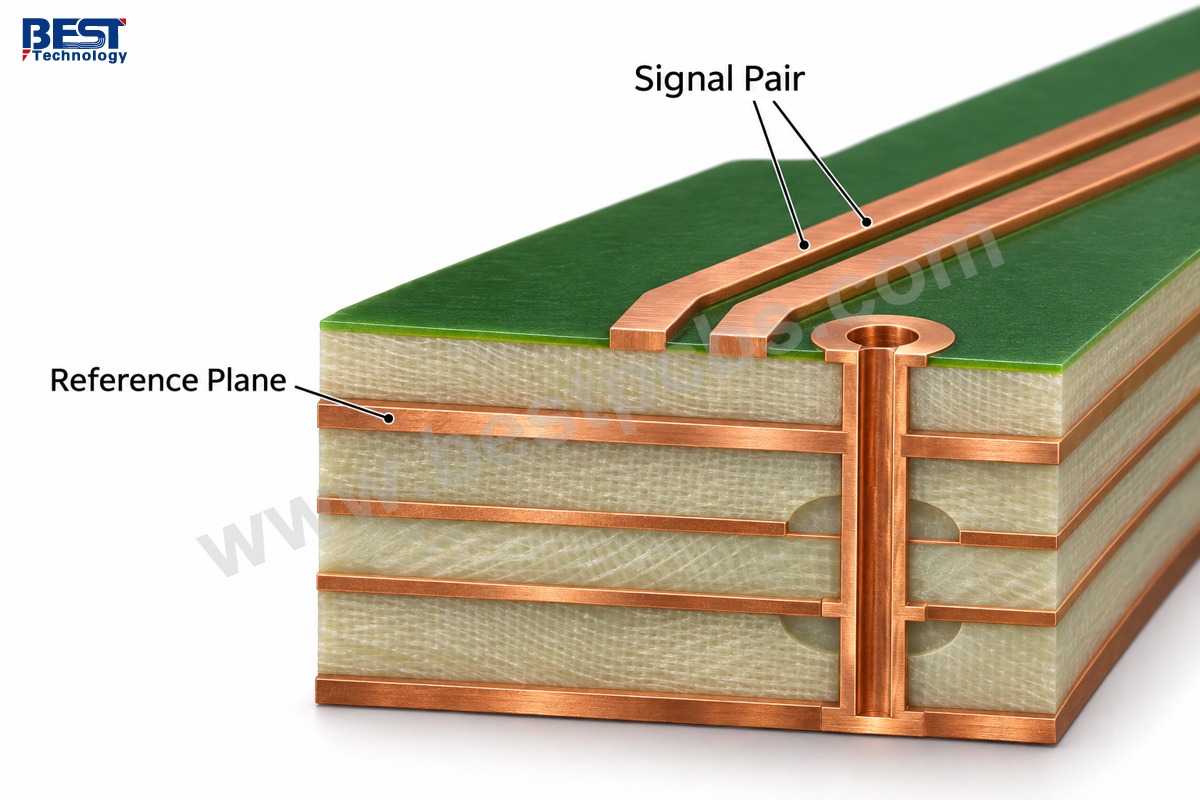
PCB cross-section showing a differential signal pair and an underlying reference plane
  • Signal routing: specify the actual laminate grade, impedance targets, routing geometry, and any required test coupons.
  • Power delivery: review copper distribution, current paths, connector interfaces, and heat concentration.
  • Dense interconnects: check BGA escape routing, via structures, solder-mask geometry, and assembly access.
  • Mechanical integration: confirm board thickness, mounting positions, stiffeners, and clearance to cooling hardware.

These are design inputs, not a claim that every AI board needs HDI, one particular low-loss material, or the same layer count. The appropriate construction follows the channel and mechanical requirements. High Tg alone is also not proof of low electrical loss.

Can Consolidation Reduce PCB Units While Increasing Board Value?

Yes. Replacing several older servers with fewer higher-capacity systems can reduce motherboard quantities while increasing PCB content or manufacturing cost per new system.

Consider an illustrative program replacing 1,000 older servers with 400 new systems after workload validation. If each system has one motherboard, the new purchase contains 400 motherboards—not 1,000. Additional accelerator, networking, and power boards may change the total, but they must be counted from the new architecture. This example is arithmetic, not a reported customer deployment or a market forecast.

Board units, fabricated area, and procurement value are separate measures. A larger board with more demanding materials, drilling, lamination, or inspection can carry a higher price without increasing unit shipments. Buyers and suppliers should state which measure they mean when discussing “PCB demand.”

Why Does Data Center Capital Spending Not Equal PCB Orders?

Data center capital spending includes buildings, power infrastructure, cooling, and other assets, so its growth cannot be converted directly into a PCB purchase-growth percentage.

Even hardware-related budgets pass through several gates before a board order is released: architecture selection, design qualification, component allocation, material approval, pilot builds, and production authorization. A site with unfinished power or cooling work may also defer installation despite an approved equipment budget.

For PCB scheduling, track the board revision, qualified stackup, pilot acceptance, firm release quantities, and material commitments. These project signals are closer to production demand than a broad infrastructure spending announcement. Separate confirmed orders from forecasts and optional releases rather than treating all three as committed factory loading.

What Should a Data Center Refresh Proposal Specify?

A data center refresh proposal should specify the workload being replaced, the retained hardware, the new board assemblies, and the qualification and rollout milestones.

  1. Define the replacement scope. Separate new systems, reused equipment, repair spares, and capacity expansion.
  2. Freeze interface and mechanical requirements. Identify connectors, power interfaces, cooling clearances, board outlines, and mounting points.
  3. Approve the manufacturing baseline. Align fabrication revision, stackup, BOM, permitted alternatives, assembly instructions, and test requirements.
  4. Qualify a pilot before volume release. Resolve board, assembly, firmware, and fixture issues against agreed acceptance criteria.
  5. Stage deliveries against deployment readiness. Match material purchases and production releases to the rollout rather than one assumed fleet replacement date.

This creates an actionable handover between system engineering and manufacturing. It also avoids comparing quotations that use different material grades, inspection coverage, or test scope.

How Can EBest Circuit Support Board Manufacturing?

We support reviewed PCB and PCBA projects through DFM, material selection discussions, fabrication, sourcing, assembly, and an agreed inspection and test plan.

For multilayer FR-4 PCB fabrication, we review the specified material system and construction rather than substituting a generic “equivalent” without approval. On assembled boards, the inspection plan can combine solder-paste inspection, AOI, BGA X-ray inspection, and functional testing according to the actual design and order scope.
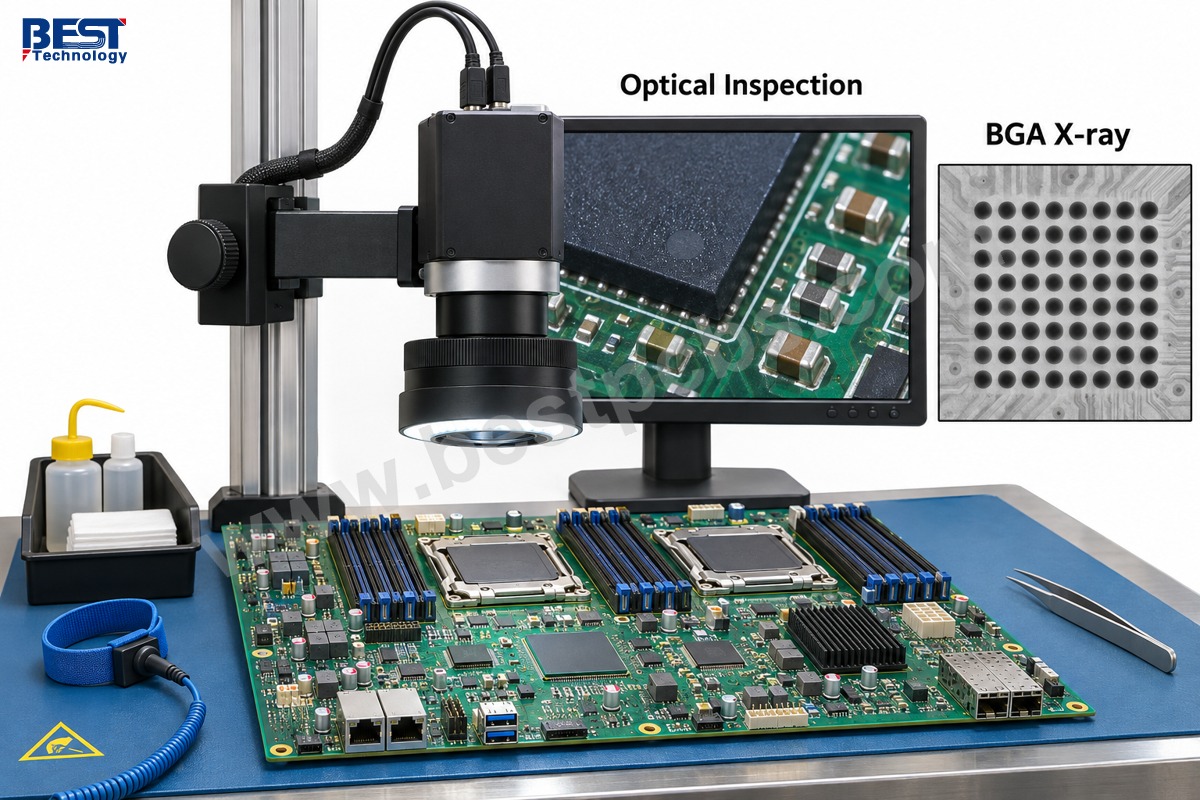
Optical inspection of a populated circuit board with a BGA X-ray comparison inset

Each method answers a different question. Bare-board electrical testing checks continuity and isolation; AOI checks visible assembly features; X-ray reveals selected hidden-joint conditions; functional testing checks defined behavior. No single inspection image proves system-level performance. We agree on the required coverage before the build so the delivered records match the project’s acceptance criteria.

FAQs About Server Refresh Cycles and PCB Demand

Does an expired server warranty mean the PCB must be replaced?

No. Warranty expiration changes support coverage, not the board’s physical condition. Replacement depends on service options, failure exposure, workload needs, and operating cost. A functioning board may remain usable, although the operator must decide whether continued service fits its reliability and security requirements.

Does a firmware upgrade create demand for new PCBs?

Not normally. Updating firmware reuses the installed hardware. New boards are needed only if the required function cannot be supported by the existing platform or if hardware modification or replacement is part of the upgrade.

Are refurbished servers the same demand source as new servers?

No. Refurbishment generally reuses existing boards, with replacement demand concentrated in failed assemblies, upgrades, or service parts. New-system manufacturing creates a different bill of materials. Combining refurbished and newly manufactured units without separating reused electronics can overstate new PCB demand.

Does every AI server require HDI PCBs?

No. HDI becomes relevant when package escape routing, interconnect density, and space constraints justify microvias or related structures. Some assemblies can use conventional multilayer construction. The board design and fabricator’s reviewed process capability determine the construction—not the AI label alone.

Should all spares be purchased with the first rollout?

Not necessarily. Spare quantities depend on service policy, repair turnaround, part availability, and the stability of the board revision. Purchasing too early can leave obsolete stock after a design change. Staged commitments can help, provided material availability and manufacturing lead times are reviewed before each release.

Plan Your Data Center Server Refresh Cycle with Manufacturing in Mind

The strongest PCB demand signal is a qualified design moving into an approved production release. If your refresh program includes custom boards, contact our engineering team at sales@bestpcbs.com. We can review the construction, sourcing, assembly, and test scope before you commit to the next build.
You may also like

Thermal Pad MCPCB: Design, Materials and Selection

October 31st, 2026

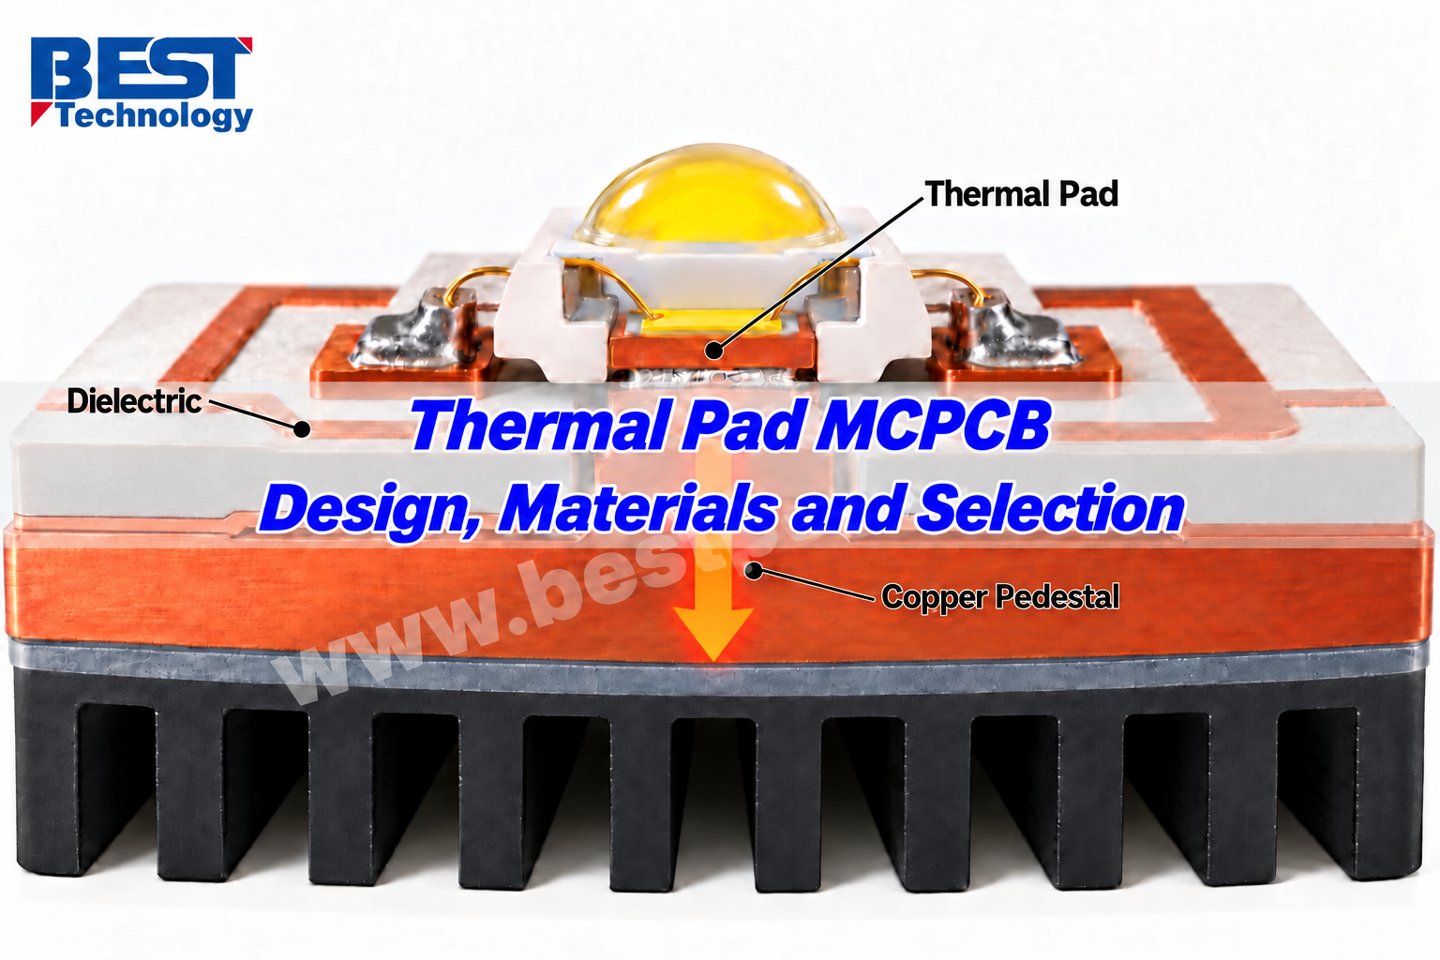
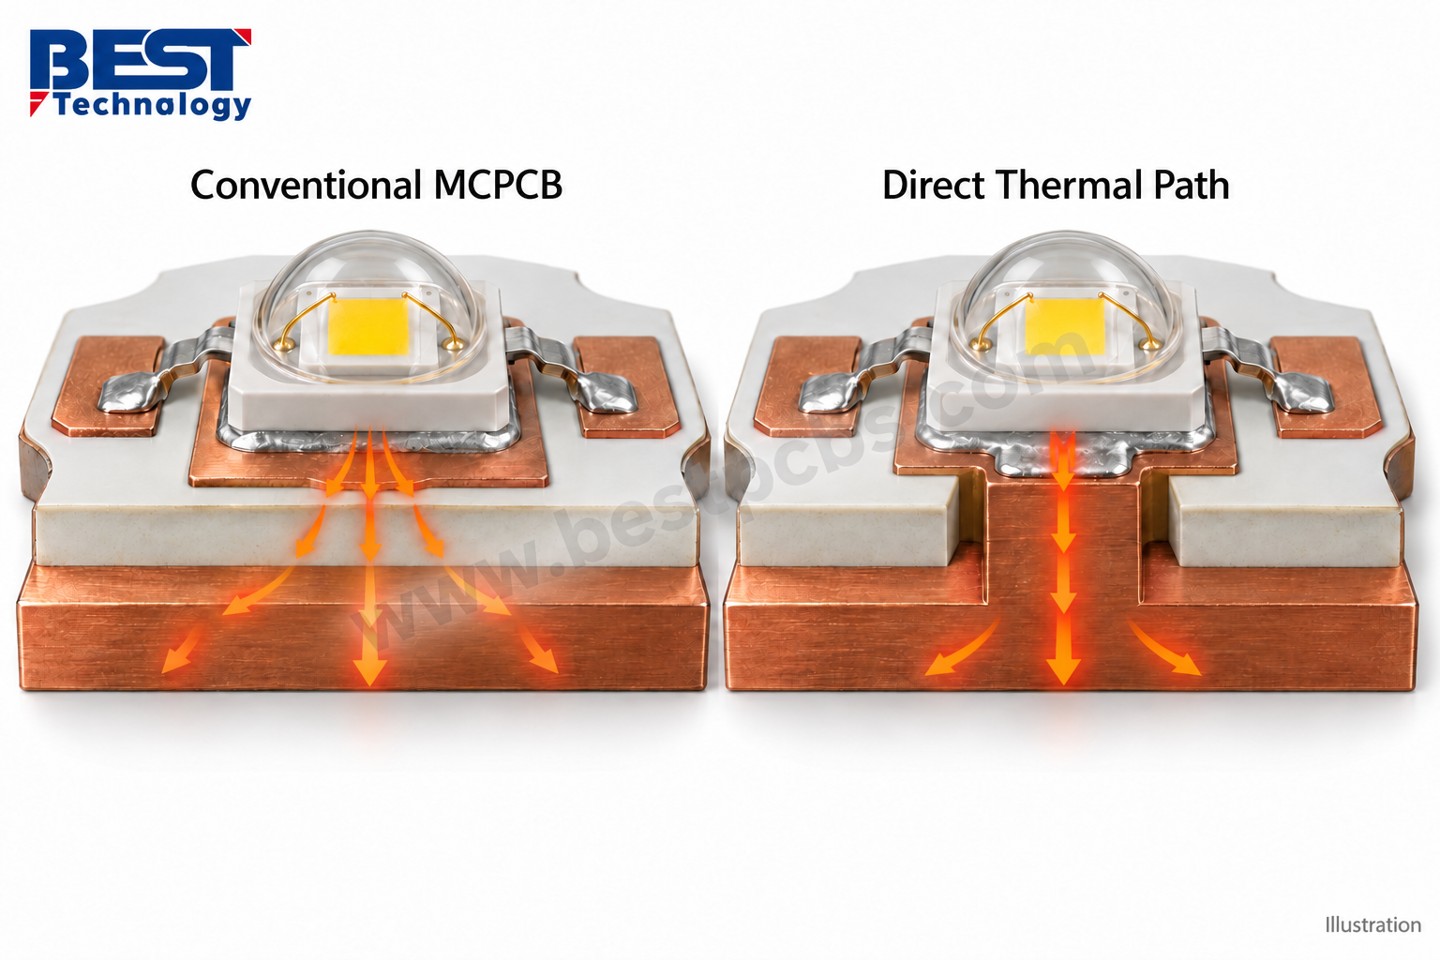
A thermal pad MCPCB commonly refers to a metal-core board that connects an LED’s thermal pad to a metal pedestal through a solder joint, bypassing the dielectric beneath that pad. This direct thermal path can reduce one part of the heat-flow resistance. It works only when the package’s electrical connections and the board’s isolation scheme allow that connection.

The first design decision is therefore electrical as well as thermal: can the LED’s heat-transfer pad safely connect to the metal base? Once that is established, compare the complete path through the package, solder, board, mounting interface and heat sink.

Conceptual 3D cutaway of an LED thermal pad soldered directly onto an integral copper pedestal, with dielectric only beneath adjacent circuit pads

Key Takeaways

  • A direct thermal path bypasses dielectric locally beneath the LED thermal pad; other circuitry still needs insulation.
  • A copper base alone does not prove that a board has a direct thermal path.
  • Dielectric thickness, conductivity and effective heat-transfer area must be considered together.
  • A board-to-heat-sink interface pad serves a different purpose from a solderable thermal land.
  • Verify package compatibility, solder quality and operating temperature before approving a stack-up.

What Does “Thermal Pad MCPCB” Mean?

In LED board discussions, the term often describes a direct-thermal-path MCPCB rather than a soft pad placed under a circuit board. A metal pedestal reaches the LED’s thermal contact location, with a soldered connection between the package and pedestal.

PCB thermal pads can refer to different parts. Three related parts are easy to confuse:

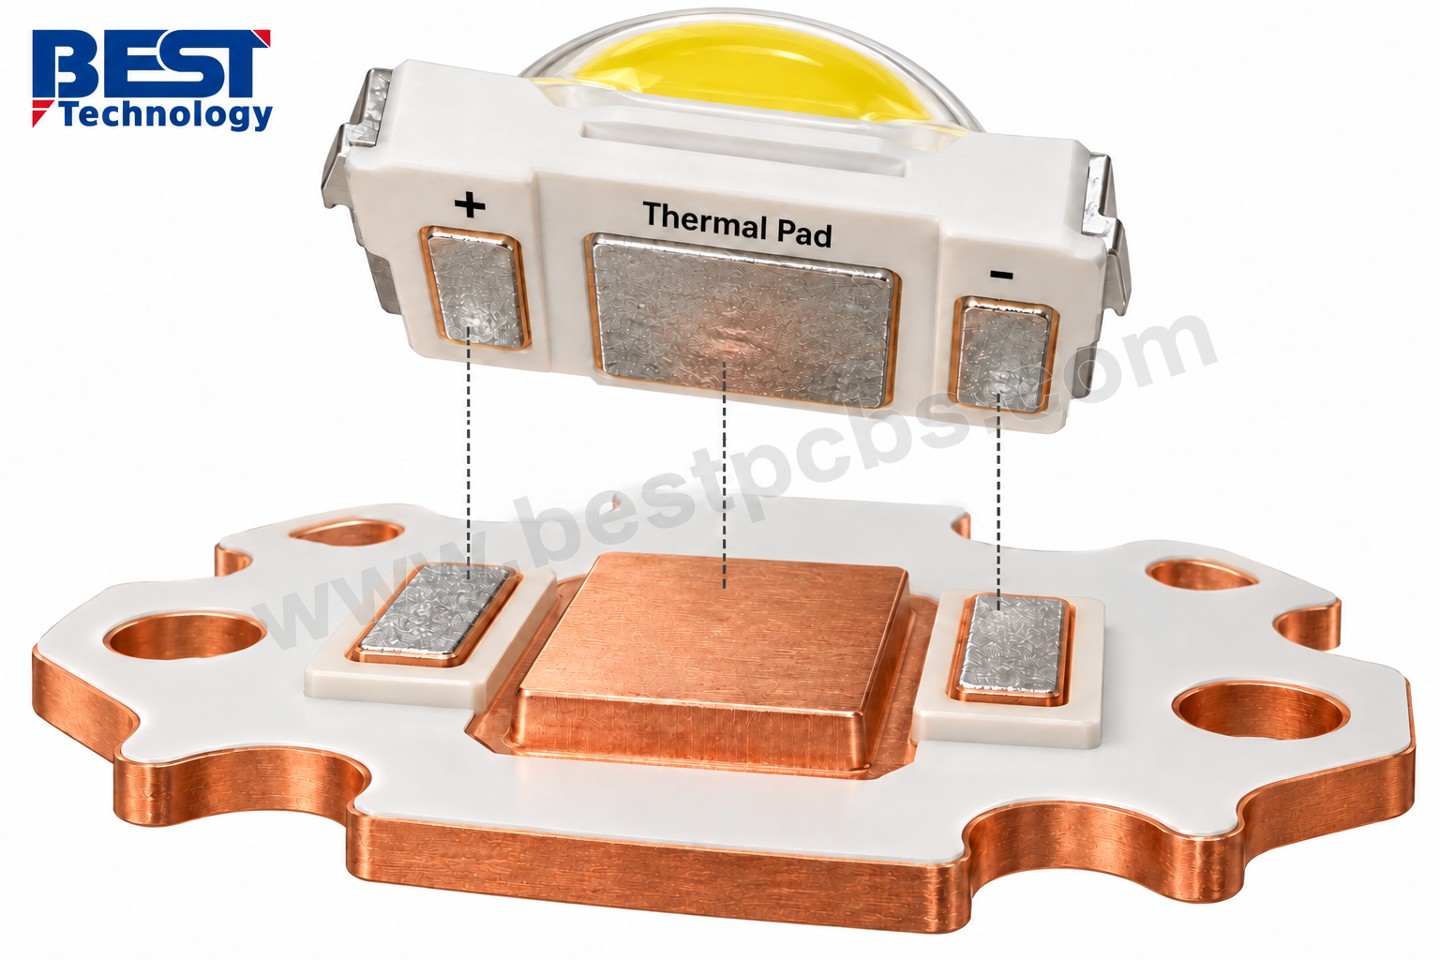
  • Package thermal pad: the exposed heat-transfer surface on the underside of the LED or component.
  • Board thermal land: the solderable surface that mates with that package pad.
  • Thermal interface pad: a separate material between the board base and heat sink.

For a thermal pad PCB, specify which one you mean on drawings and quotation requests. Asking for a “thermal pad” without a cross-section can result in a different construction from the one intended.

Generic LED underside and matching DTP board showing separate anode, neutral thermal pad and cathode contacts

How Does a Direct Thermal Path Differ from a Conventional MCPCB?

A conventional insulated MCPCB carries heat through its dielectric before it reaches the metal base. A direct thermal path bypasses that dielectric at the designated thermal contact while retaining electrical insulation beneath the surrounding circuit.

Cree LED describes heat flowing from the LED package through its thermal pad into the PCB and onward to a heat sink. Adura’s SinkPAD description explains the local dielectric bypass and specifies compatibility with electrically neutral thermal pads. Neither principle makes every LED package interchangeable.

At EBest Circuit, we provide metal-core PCB manufacturing and PCB assembly services. For a thermal-pad design, send the LED part number and proposed stack-up together so we can review the board and assembly requirements against the same package information.

Conceptual 3D cross-sections comparing continuous dielectric beneath a conventional MCPCB thermal land with a direct copper pedestal path

Which Material Parameters Should You Compare?

Compare dielectric thickness and dielectric thermal conductivity on the same basis before comparing material grades. A conductivity value for a metal base or a complete test structure cannot simply replace the dielectric value.

The following published Henkel/Bergquist examples describe Thermal Clad dielectric grades. They are reference material data, not measured performance or confirmed stock for an EBest Circuit board.

Dielectric Grade Thickness (µm) Dielectric k (W/m·K)
HT-04503 76 2.2
HT-07006 152 2.2
MP-06503 76 1.3

Source and conditions: Henkel/Bergquist’s Thermal Clad Comprehensive Selection Guide, dielectric selection table. Thickness uses an optical method; dielectric conductivity uses extended ASTM D5470. Values are published reference characteristics. The table does not provide a temperature-specific curve, so these numbers should not be treated as guaranteed across the operating range.

HT-04503 and HT-07006 illustrate why thickness matters: their listed dielectric conductivity is the same, but their thickness differs. MP-06503 provides a same-thickness comparison with HT-04503. Confirm the current grade, construction and applicable data sheet before ordering.

When Should You Choose a Conventional or Direct-Path Board?

Choose a conventional insulated MCPCB when its verified thermal performance and electrical isolation meet the design. Evaluate a direct-path structure when resistance beneath a compatible package pad is a significant part of the thermal budget.

Selection Point Conventional MCPCB Direct Thermal Path
Below the thermal land Dielectric separates land and base Metal connection bypasses dielectric locally
Electrical relationship Land remains isolated by the specified dielectric Thermal contact connects electrically to the base
Package suitability Depends on isolation and heat budget Requires a compatible pad connection and geometry
Primary selection trigger Specified isolation and temperature target are met Local dielectric resistance needs reduction
Heat-sink interface Still needs a suitable mounting interface Still needs a suitable mounting interface

A direct-path board does not remove the package’s internal thermal resistance or the heat sink’s limits. If the dominant problem is a poor mounting interface or inadequate cooling to ambient, changing the board alone may deliver little improvement. Compare alternatives with the same LED, heat load, mounting arrangement and ambient conditions.

How Can You Estimate Dielectric Thermal Resistance?

For a uniform layer carrying heat straight through its thickness, estimate MCPCB thermal resistance with R = t / (k × A). Use thickness t in metres, conductivity k in W/m·K and area A in m²; the result is K/W.

Calculated example, not a test result: assume a 100 µm dielectric, conductivity of 2 W/m·K and a uniform 5 × 5 mm heat-transfer area.

  • t = 0.0001 m
  • A = 0.005 × 0.005 = 0.000025 m²
  • R = 0.0001 ÷ (2 × 0.000025) = 2 K/W
  • At an assumed 3 W of heat crossing that layer, ΔT = 3 × 2 = 6 K.

This simplified calculation excludes lateral spreading, solder and mounting contact resistance, package resistance, temperature-dependent properties and parallel heat paths. It is useful for comparing variables, not predicting an assembled LED’s junction temperature. Use heat dissipated into the path, rather than automatically treating all electrical input as heat.

How Should You Define the Thermal Pad and Electrical Isolation?

PCB thermal pad design starts with the exact component’s recommended land pattern and pad connection. There is no universal MCPCB thermal-pad size that fits every LED with the same external package dimensions.

  1. Identify the pad’s electrical function. Confirm whether it is neutral, connected to an electrical terminal, or subject to a specified connection requirement.
  2. Match the footprint. Check the thermal contact, anode, cathode, orientation and clearances against the current package drawing.
  3. Define the cross-section. Show where dielectric remains and where the thermal contact joins the metal base.
  4. Review the enclosure connection. Decide whether the base is floating, grounded or connected mechanically to conductive parts.
  5. Approve assembly geometry. Confirm pedestal height, coplanarity and solder-joint requirements with the board and assembly teams.

Do not connect an electrically active thermal pad to a common metal base merely because the footprint fits. An unexpected base connection can change the circuit or create a short. Package documentation and the approved isolation design take priority over a generic board drawing.

Does a Direct-Path MCPCB Still Need Thermal Interface Material?

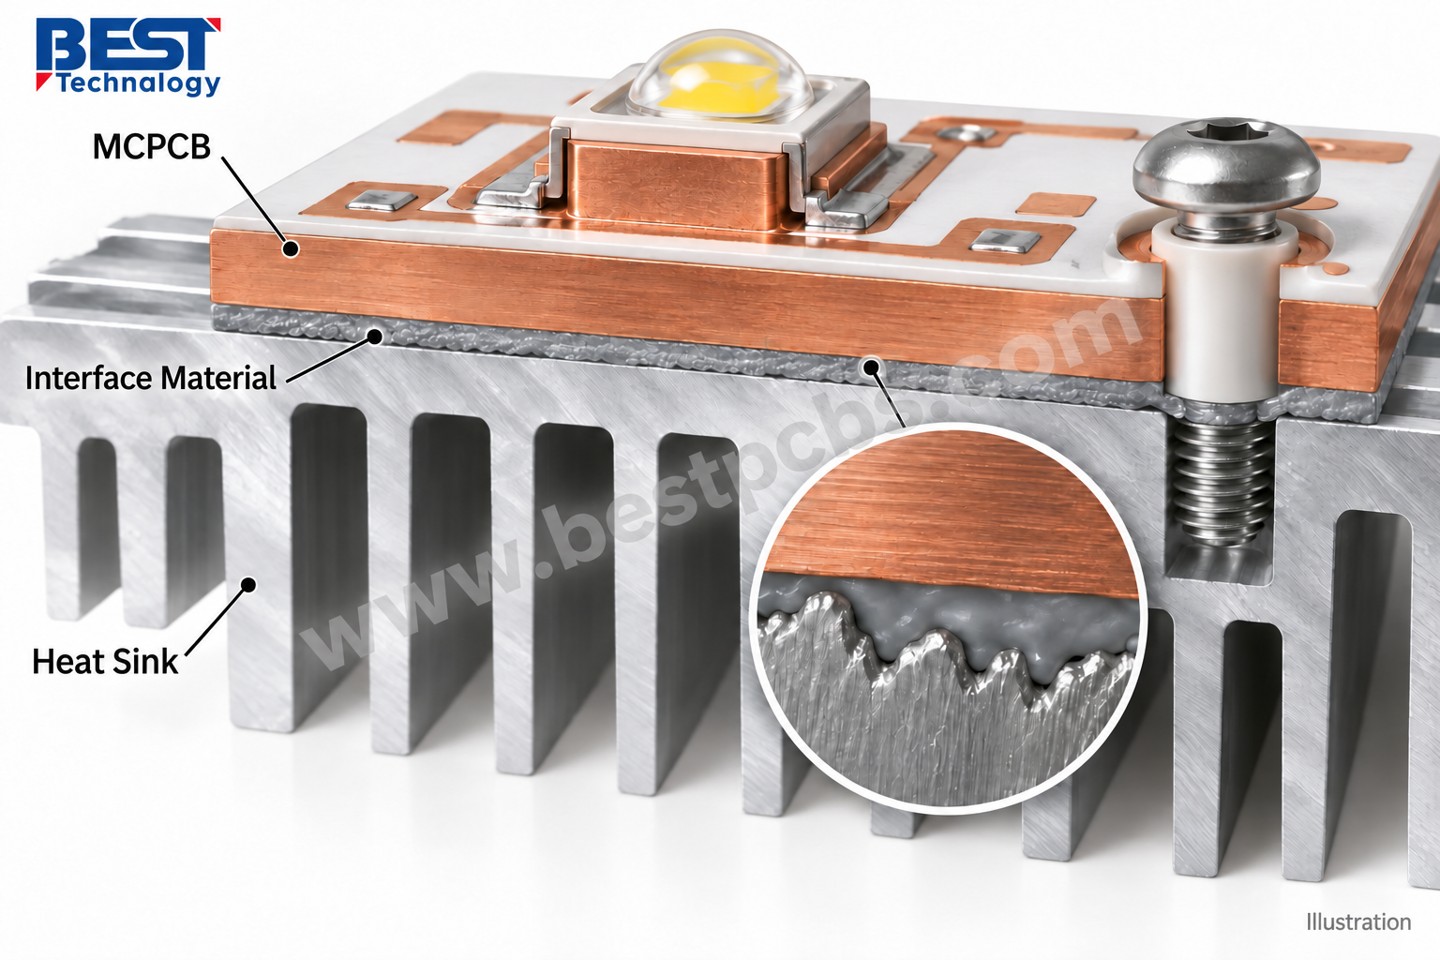
It may still need interface material between the metal base and heat sink because a direct path inside the board does not eliminate the separate mounting interface.

Choose an interface for the actual gap, surface flatness, clamping arrangement and electrical isolation requirement. A compliant pad may accommodate a gap that a thin grease layer cannot; adding unnecessary thickness can also increase resistance. Use the interface supplier’s pressure and thickness data for the selected product.

Do not insert a soft gap pad into a location designed for a soldered LED thermal contact. Those materials perform different jobs and require different assembly conditions.

Conceptual MCPCB mounting cutaway showing the interface material between the metal base and aluminum heat sink, with an insulated mounting screw

How Do You Verify the Assembled Thermal Path?

Verify electrical isolation and operating temperature in the final mounting arrangement; a successful continuity test alone does not establish thermal performance.

  • Before assembly: compare the approved stack-up, package drawing, thermal contact location and circuit isolation.
  • During assembly validation: confirm paste deposition, placement and a reflow profile suitable for the component and board. Use supplier guidance rather than a universal temperature setting.
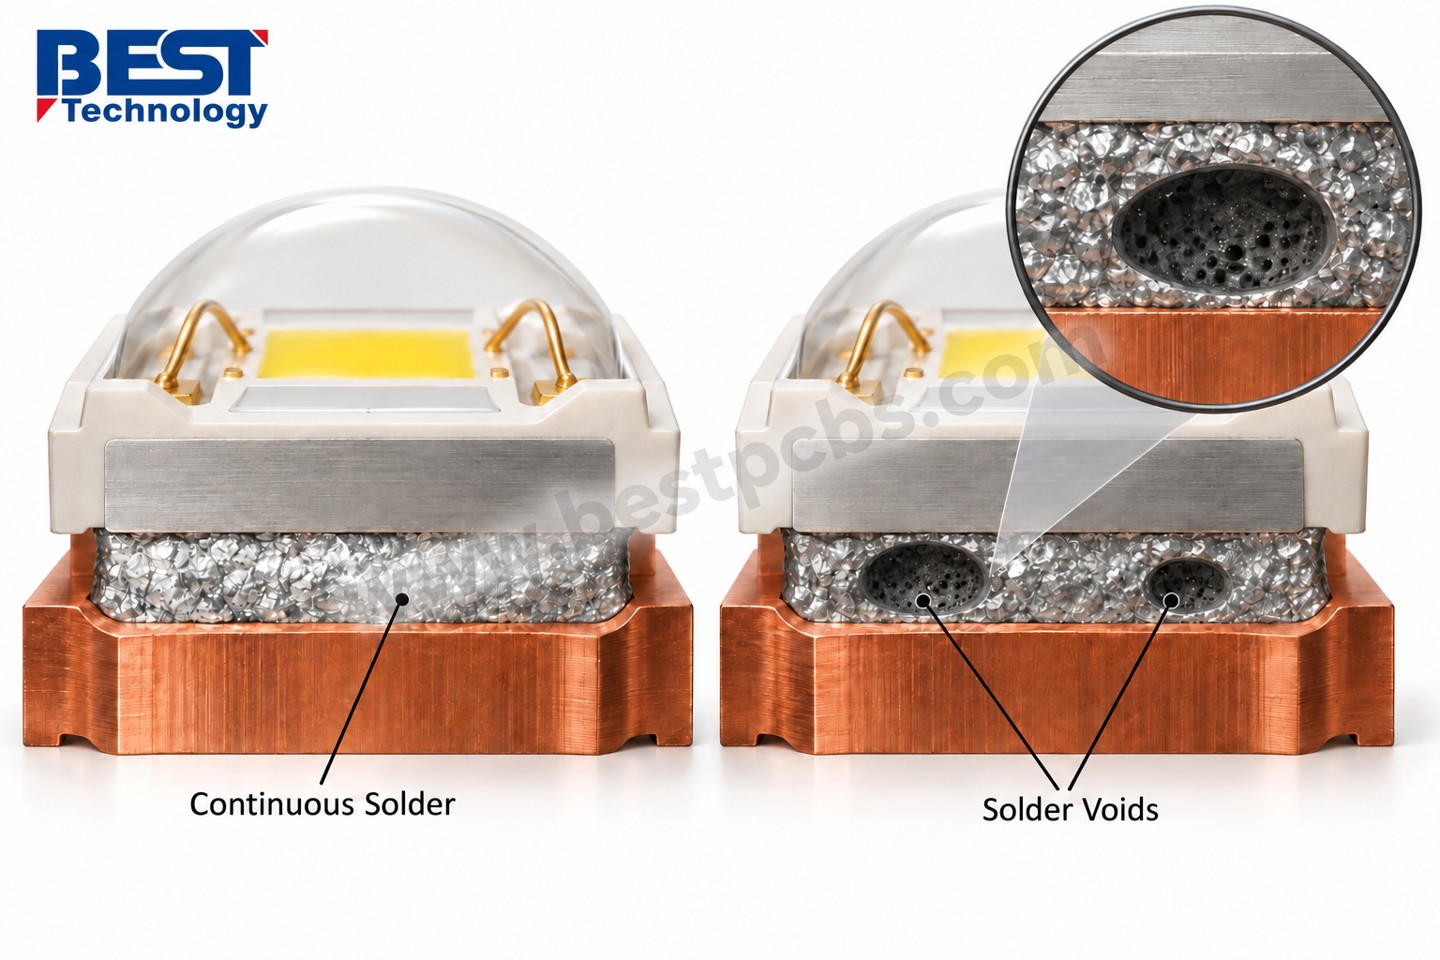
  • After reflow: inspect hidden solder contacts with an appropriate method. Define voiding criteria for the actual package and application; do not adopt an unsupported universal percentage.
  • During operation: record ambient conditions, drive current, mounting pressure or torque, interface material and measurement location. Run until temperatures stabilize.
  • Before release: compare measured values and any junction-temperature estimate with the component’s specified limits and the project’s approved margin.

Stop the test if temperature exceeds the approved limit, rises abnormally, or electrical isolation fails. Review the suspected cause, make a controlled correction and repeat the same test conditions. An infrared image can locate a hot region, but it does not by itself prove the junction temperature or the cause of overheating.

Conceptual cross-sections comparing continuous solder contact with enclosed solder voids beneath an LED thermal pad; not a real inspection image

What Should You Send Us for a Thermal Pad MCPCB Review?

Send the LED part number, manufacturing files and mounting details so we can assess the intended heat path and board requirements together.

  • Gerber files, board outline and a proposed cross-section.
  • LED data sheet, land pattern and thermal-pad electrical connection.
  • Base material, dielectric grade and thickness, copper weight and surface finish.
  • Heat load or operating conditions, temperature target and heat-sink interface.
  • Quantity, assembly scope and required electrical and thermal checks.

For related construction options, see our direct-thermal-path board page. Email the project files to sales@bestpcbs.com. We will review the requested structure; material availability, pad geometry and acceptance requirements need confirmation for the actual design.

You may also like

Specialized Semiconductor Packaging and Testing Companies List

October 29th, 2026

This specialized semiconductor packaging and testing companies list includes ASE Technology Holding, Amkor, JCET, Powertech, Tongfu, Huatian, ChipMOS, Hana Micron and UTAC. These providers operate in semiconductor back-end manufacturing: connecting and protecting dies, then testing devices against electrical requirements. Their portfolios differ across memory, logic, RF, power and multi-die integration. Choosing a provider starts with the device, package and test flow—not a company’s name alone.

At EBest Circuit, we work at the downstream PCB and PCBA stage. We help customers manufacture circuit boards and assemble packaged components; we are not presenting ourselves as an OSAT provider. Understanding the package handoff helps our customers prepare the footprint, assembly process and board-level tests correctly.

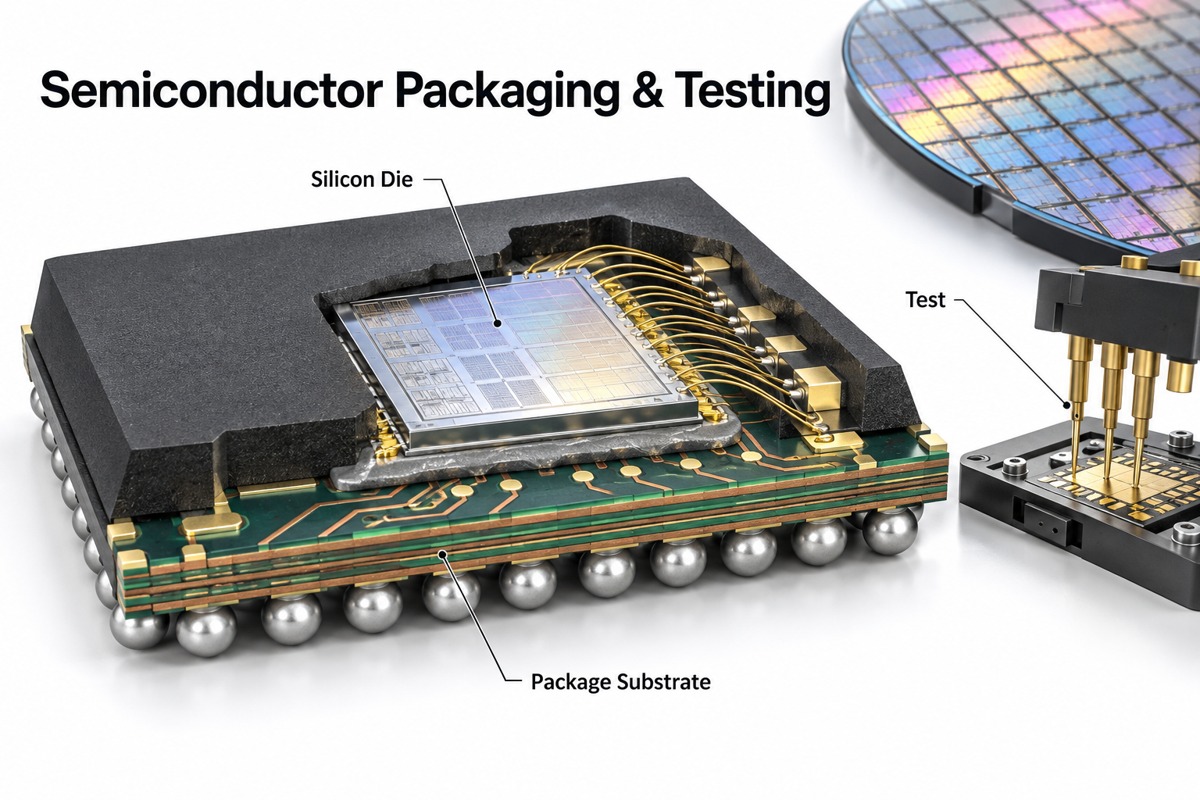
Semiconductor package cutaway showing silicon die, package substrate and testing context

Key Takeaways

  • OSAT means outsourced semiconductor assembly and test; the assembly is primarily at die and package level.
  • The list covers nine providers with publicly documented packaging and test services, not a revenue ranking or an endorsement.
  • ASE and SPIL belong under ASE Technology Holding; counting them separately can duplicate a corporate group.
  • Memory, display-driver, power, RF and advanced multi-die products require different package and test capabilities.
  • Wafer probe, final test, burn-in and system-level test serve different purposes; confirm the required flow and site.
  • Semiconductor package qualification does not replace PCB assembly inspection or finished-board functional testing.

Which Companies Offer Packaging and Test?

ASE Technology Holding, Amkor, JCET, Powertech, Tongfu, Huatian, ChipMOS, Hana Micron and UTAC provide packaging and test services with different technology and application emphases. The following list of semiconductor packaging companies summarizes those distinctions.

Provider Publicly described service focus
ASE Technology Holding, including ASE and SPIL Broad package assembly, testing and heterogeneous integration
Amkor Technology Package development, wafer bumping, assembly and multiple test stages
JCET Group Package design, integration, assembly and testing
Powertech Technology (PTI) Memory and logic probing, packaging, final test and module services
Tongfu Microelectronics Packaging and test for computing, communications, automotive and other devices
Huatian Technology Leadframe, memory, SiP, wafer-level and fan-out services
ChipMOS Technologies Display-driver, memory and mixed-signal back-end services
Hana Micron Bumping, wafer test, assembly, final test and modules
UTAC Group Leadframe, laminate, wafer-level, SiP, power and test services

Scope checked against public company materials on October 29, 2026. Inclusion does not establish that every plant supports every package, that capacity is available, or that a supplier accepts a particular prototype quantity.

What Does Each Provider Focus On?

The useful differences are each provider’s package portfolio, device experience and test coverage. The summaries below explain where to begin a technical discussion without treating the suppliers as interchangeable.

ASE Technology Holding

ASE Technology Holding brings together ASE, SPIL and USI. ASE’s semiconductor services include package design, assembly and test, while its heterogeneous-integration work addresses combinations of dies and components in a package. SPIL is part of the same holding group, not a separate independent group entry in this list.

For sourcing, identify the operating company and qualified site behind the proposal. A group-level technology presentation is not a site-specific production approval.

Amkor Technology

Amkor offers package design support, characterization, wafer bumping, assembly and test. Its published test portfolio includes wafer probe, final test, burn-in and system-level test, with applications covering compute, communications, automotive, memory and other device types.

Its breadth makes the test strategy part of the package discussion. Define whether the project needs wafer-level screening, post-package electrical coverage, operating-temperature testing or a system-level insertion.

JCET Group

JCET describes an integrated service chain covering packaging design, system integration and testing. It is a provider to evaluate when package development and assembly/test execution need to be coordinated rather than purchased as unrelated steps.

For a multi-die project, request the proposed interconnect architecture, thermal model and package-to-board interface. Do not assume that an advanced-platform name identifies one fixed structure or a universally available production line.

Powertech Technology

Powertech, commonly abbreviated PTI, publishes services for chip probing, wafer-level packaging, flip-chip packages, wire-bond BGA, SiP and module assembly. Its final-test coverage explicitly includes DRAM, NOR flash, NAND flash, multi-chip packages and logic devices.

Memory projects should match the provider’s test platform to the actual device generation and organization. Package compatibility alone does not prove test-program readiness or the required parallel-test throughput.

Tongfu Microelectronics

Tongfu publishes services from design simulation and wafer testing through packaging, final test and system-level test. Its stated application coverage includes computing, communications, automotive, memory and other semiconductor categories.

For a compute device, discuss package routing, power delivery, thermal control during test and the required test stages together. A high-power device may need specialized handling and temperature management beyond a standard final-test setup.

Huatian Technology

Huatian’s public portfolio includes SiP, memory, MEMS and wafer-level fan-out packaging. Its test services cover program development, wafer probing, final test and system-level test.

This range spans very different manufacturing flows. Confirm whether the proposal is for a leadframe package, substrate-based package or wafer-level architecture, and which site will perform the work.

ChipMOS Technologies

ChipMOS focuses on back-end services for display-driver ICs, memory and mixed-signal devices. Its published assembly portfolio includes leadframe and organic-substrate packages, with bumping and display-related interconnect services.

A display-driver project should specify whether its interface is chip-on-film, chip-on-glass or another format. Those interfaces are not interchangeable with an ordinary board-mounted BGA or QFN.

Hana Micron

Hana Micron describes a turnkey service chain including bumping, wafer probe, assembly, final test and modules. Its materials discuss a memory-packaging base and expansion into non-memory packaging and test.

Match the inquiry to a documented package family and test requirement. Do not turn a development roadmap into an assumption that a particular advanced package is already qualified for the intended product.

UTAC Group

UTAC publishes leadframe, laminate, SiP, wafer-level, MEMS/sensor and power-package services, alongside wafer sort, final test, test development and reliability services.

For analog, mixed-signal, sensor or power products, define the electrical stimulus, measurement limits and thermal conditions early. Specialized semiconductor testing and packaging companies need device-specific coverage, not simply a request to “test all chips.”

What Is an OSAT Company?

An OSAT company is an outsourced semiconductor assembly and test provider that turns semiconductor dies into tested packages or performs selected stages of that back-end flow. Customers may be fabless chip companies, integrated device manufacturers or other semiconductor businesses.

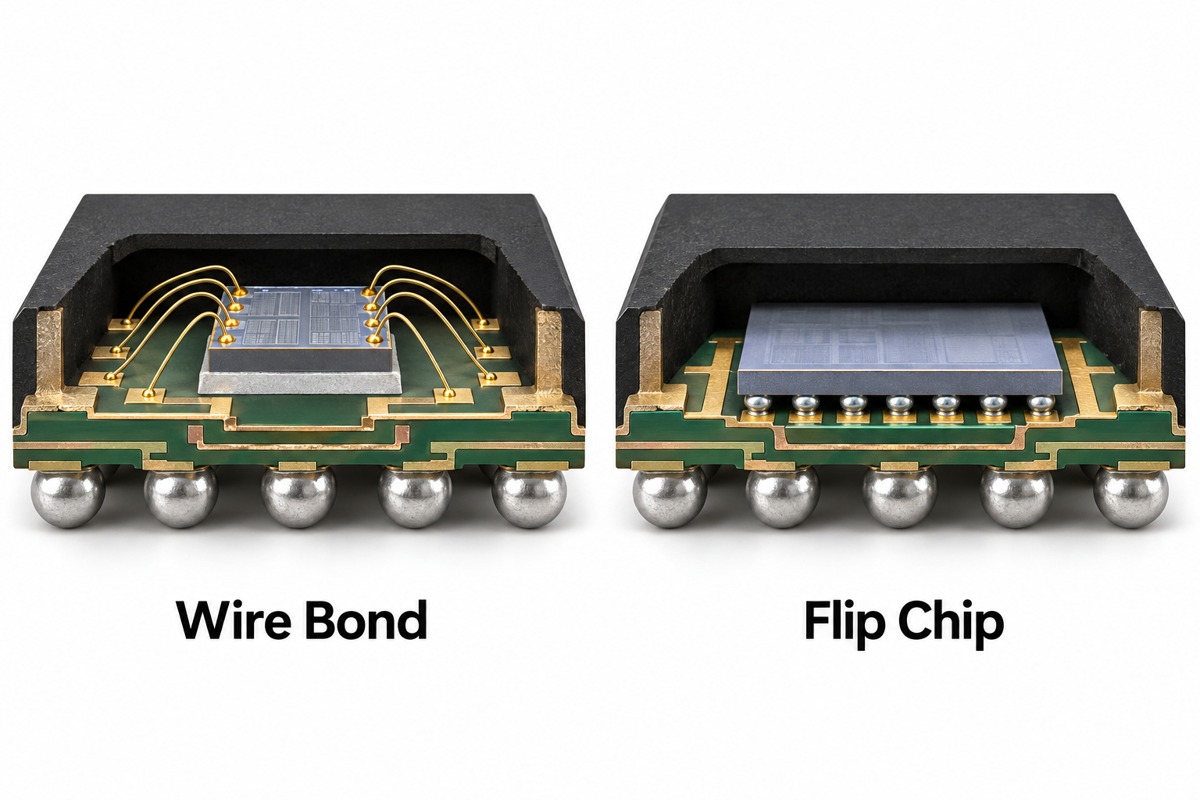
Semiconductor chip packaging companies connect die pads to the package’s external terminals and protect the die mechanically. Depending on the architecture, the connection can use bond wires, flip-chip bumps, redistribution layers, interposers or combinations of these structures.

For a closer explanation of package construction, see our IC packaging guide. Packaging is not the same operation as fabricating the transistors on a wafer, although wafer-level packaging can involve processes performed on a wafer before singulation.

Wire-bond and flip-chip package cross-sections showing different die interconnections

Which Semiconductor Test Services Are Different?

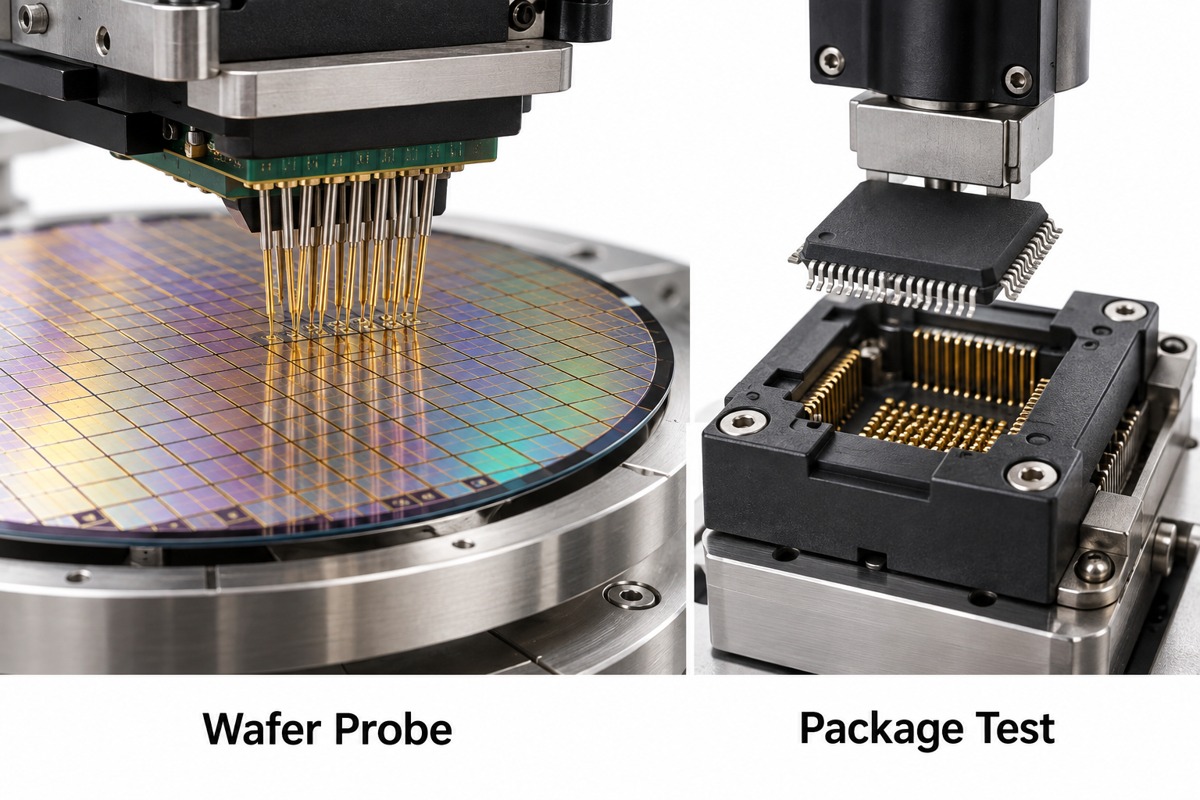
Wafer probe checks dies before packaging, final test checks packaged devices, burn-in applies a specified stress screen, and system-level test exercises devices in a more application-like environment. They are complementary stages, not different names for the same inspection.

Test stage Test object Main purpose
Wafer probe or wafer sort Dies on a wafer Electrical screening and binning before assembly
Final test Packaged device Verify specified electrical and functional limits
Burn-in Wafer or packaged devices, depending on flow Apply defined voltage/temperature stress screening
System-level test Device in a test system Exercise application-like workloads or interactions
Reliability qualification Specified samples and structures Evaluate a defined qualification plan

“100% tested” needs a definition: which units, which parameters, at what temperature, with which guardbands and test limits? It does not mean every possible failure mechanism has been eliminated. Qualification sampling also differs from production screening.

Wafer probing equipment and a packaged IC test socket illustrating separate test stages

How Do Advanced Packaging Providers Differ?

Compare advanced semiconductor packaging companies against the actual package architecture, interconnect requirements, thermal load and qualification status—not the word “advanced” in a brochure.

  • Architecture: wire bond, flip chip, fan-out, SiP, 2.5D or 3D integration.
  • Physical interface: die dimensions, die-to-die connections, external ball map and package outline.
  • Electrical behavior: power distribution, signal bandwidth and parasitic models.
  • Thermal and mechanical behavior: cooling interface, warpage, materials and stress.
  • Production evidence: qualified site, process maturity, test coverage and change-control responsibilities.

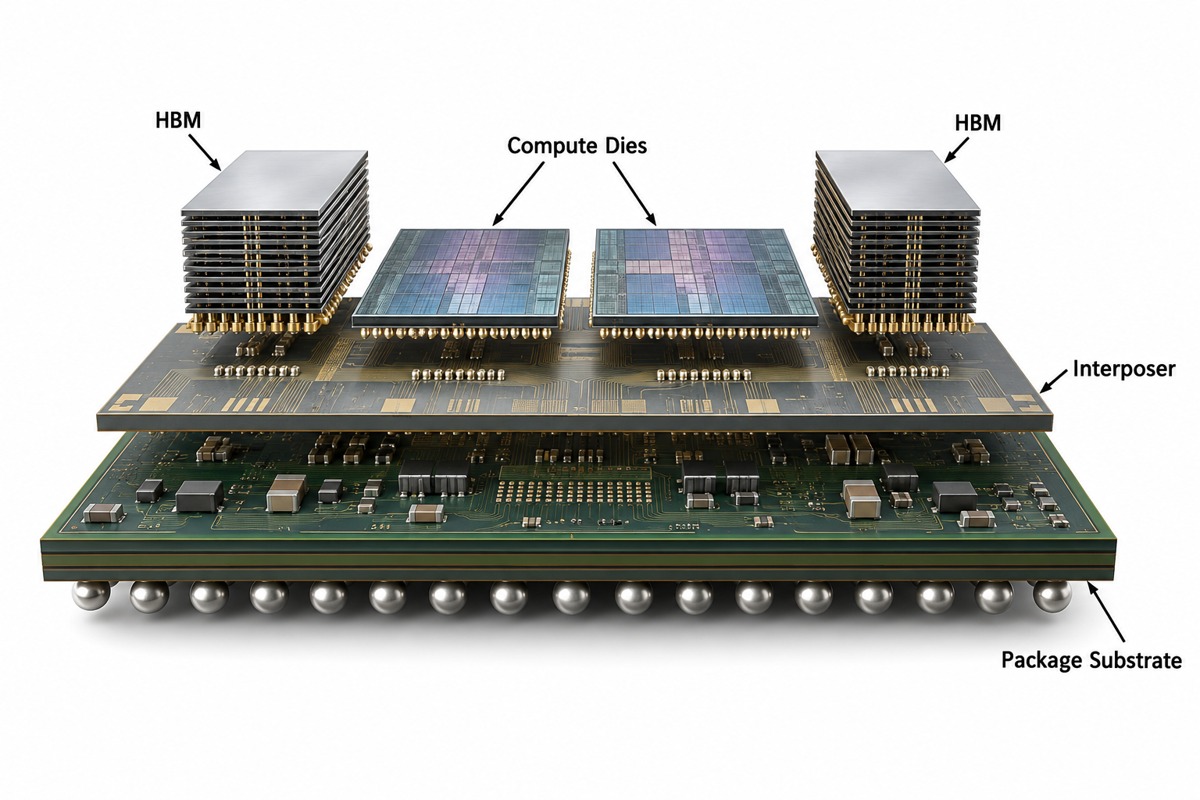
For example, a multi-die logic-and-HBM package needs short, dense package-level connections and coordinated power and thermal design. A small power package may instead prioritize its current path, heat flow and isolation requirements. The same supplier can address both through different technology platforms and production flows.

Illustrative multi-die package structure with compute dies, HBM, interposer and package substrate

What Should You Confirm Before Choosing an OSAT?

Confirm the package, qualified manufacturing site, test ownership, capacity arrangement and commercial scope before selecting a provider. A public service portfolio is a starting point, not an accepted manufacturing commitment.

  1. Define the incoming material: wafer, singulated die, known-good die or partly processed assembly.
  2. Agree on the package drawing, materials and interconnect architecture.
  3. Assign responsibility for test development, sockets, load boards and correlation.
  4. Document qualification, traceability, failure-analysis access and change notification.
  5. Separate development tooling and non-recurring engineering from recurring production charges.
  6. Confirm available capacity, minimum order terms and the transition from engineering lots to production.

Choose the technical flow first, then compare like-for-like quotations. The lowest unit assembly price may exclude test development, substrate tooling or another required step.

How Is OSAT Different from PCB Assembly?

OSAT primarily connects bare semiconductor dies into packages; PCB assembly solders packaged components and other parts onto a circuit board. The two stages have different inputs, equipment and acceptance tests.

Item Semiconductor packaging and test PCB assembly
Typical input Wafer or bare dies Bare PCB and electronic components
Interconnect Bond wires, microbumps or package routing Solder joints, connectors and board traces
Typical output Tested IC package or module Populated circuit board
Acceptance focus Package integrity and device specifications Assembly quality and board functions

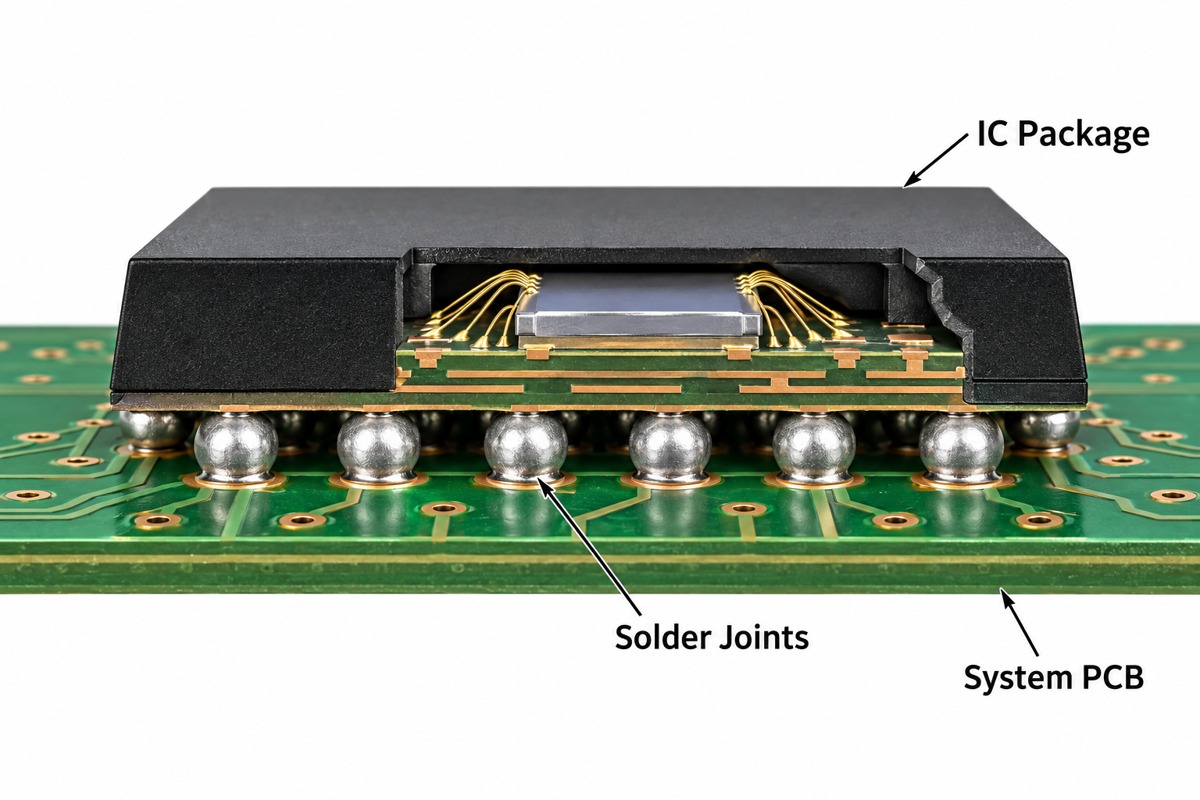
At the handoff, the board designer needs the exact package drawing, recommended land pattern, moisture-sensitivity handling and allowed assembly profile. Internal die-to-die bump pitch must never be used as the PCB’s external pad pitch.

Our PCB assembly services address that board-level stage. Device test results do not replace inspection of the solder joints or verification of power, firmware and interfaces on the finished board.

Semiconductor IC package connected through solder joints to a larger system PCB

FAQ About Semiconductor Packaging and Testing Companies

Are foundries and OSAT providers the same?

No. Foundries primarily manufacture semiconductor wafers, while OSATs specialize in outsourced assembly and test. Some foundries also offer advanced packaging, so compare the specific service rather than assume one company type has only one capability.

Should ASE and SPIL be counted separately?

They can be discussed as operating businesses, but both are within ASE Technology Holding. This list treats the holding group as one entry to avoid presenting two group businesses as independent corporate alternatives.

Can a small hardware company order a few packaged custom chips?

Acceptance depends on the provider, technology and project terms. Engineering support, tooling and test-program development may dominate a small lot’s cost. Confirm the minimum engagement and development scope directly instead of assuming prototype-PCB ordering terms apply.

Does every OSAT provide leading-edge 2.5D packaging?

No. A provider may specialize in leadframe packages, memory, display drivers or other products. Even when advanced packaging is advertised, verify the particular architecture, site and qualification status for your device.

Do packaging providers make the package substrate themselves?

Not necessarily. The substrate can come from a specialist supplier and be integrated by the package assembler. Clarify who owns substrate design, supplier qualification, procurement and incoming inspection.

Does passing chip final test guarantee a working PCBA?

No. Board-level faults can still arise from soldering, power delivery, incorrect parts, firmware or interface design. A working assembly requires its own inspection and functional acceptance plan.

How Can EBest Circuit Support Your PCBA?

We support PCB fabrication, component sourcing and PCBA after the semiconductor package interface is defined. Our review connects the package land pattern to board construction, assembly access and the agreed functional tests.

If you are integrating packaged ICs into a new product, contact sales@bestpcbs.com. We can review the board-manufacturing and assembly scope, while the semiconductor packaging provider remains responsible for its die-level process and package qualification.

You may also like

Guitar Effects PCB: Layout, Assembly and Audio Testing

October 29th, 2026

A guitar effects pcb is the printed circuit board inside a guitar pedal that connects its audio-processing components, power circuit and control interfaces. It may implement overdrive, fuzz, filtering, delay or another effect. A dependable board needs more than a correct schematic: input routing, return-current paths, supply filtering and enclosure fit determine whether the finished pedal is quiet, stable and practical to assemble.

At EBest Circuit, we support custom PCB fabrication and PCB assembly from customer-approved designs. For effects projects, we review footprints, polarity markings, control alignment and test access before manufacturing. Circuit ownership and permission to use a design remain separate from the fabrication process.

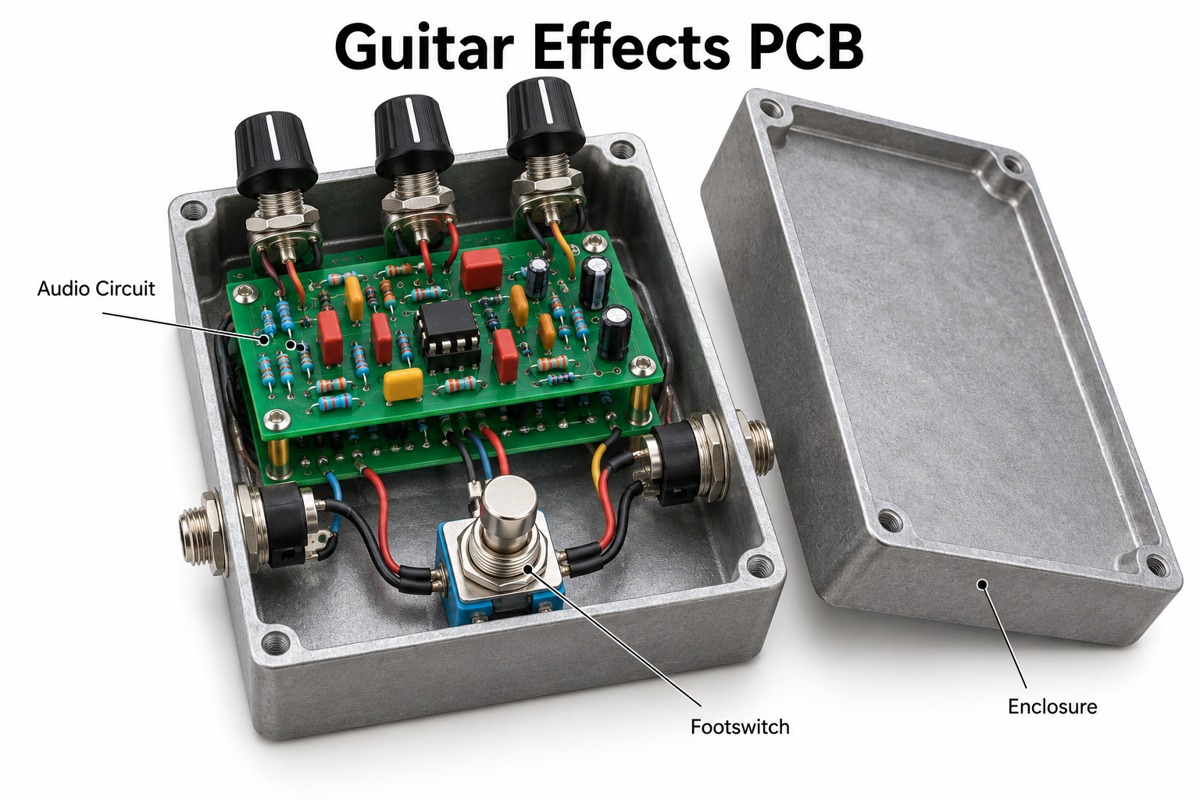
Open guitar pedal enclosure showing its effects PCB, footswitch and controls

Key Takeaways

  • A pedal PCB carries the audio circuit; a pedalboard holds complete pedals and is a different product.
  • Place the input, gain or processing stages and output in signal-flow order, with noisy power and switching nodes kept away from sensitive inputs.
  • A 9 V supply does not mean every op amp can handle every signal on that rail. Verify input common-mode range, output swing and biasing.
  • Two-layer FR-4 is a practical starting point for many analog pedals; digital effects may need more routing and power-plane resources.
  • Through-hole, SMT and mixed assemblies can all work. Component values, packages and circuit behavior matter more than assembly style alone.
  • Verify the PCB in its real enclosure, then test DC conditions, audio response, bypass operation and noise.

What Does a Guitar Effects PCB Do?

The PCB connects components that change a guitar signal’s level, frequency response, waveform or timing, while distributing power and carrying control connections.

Effect Circuit function Layout priority
Boost Raises signal level Input loading and output headroom
Overdrive or distortion Amplifies and clips the waveform Feedback-loop length and input/output separation
Fuzz Uses nonlinear gain stages Transistor bias and leakage-sensitive nodes
EQ or filter Changes frequency response RC values and control wiring
Delay or modulation Processes a time-varying or delayed signal Clock coupling, power filtering and mixed-signal returns

A PCB sold as a bare board contains no assembled components unless explicitly stated. A kit may add parts, while a PCBA is a populated circuit board. None of these terms automatically includes an enclosure, firmware or final audio testing.

Guitar Pedal PCB Schematics

Guitar pedal PCB schematics define the electrical connections, component values, bias network and switching arrangement that the layout must preserve. They do not define the enclosure geometry or every manufacturing detail.

Before placing parts, confirm:

  • Input and output impedance targets and the expected signal amplitude.
  • Supply voltage, connector polarity and reverse-polarity protection.
  • Op-amp or transistor pin assignments for the exact package.
  • Ground, midrail reference and any negative supply as distinct nets.
  • Potentiometer values, tapers and terminal numbering.
  • Bypass switching and LED control connections.

For example, a non-inverting stage with a 100 kΩ feedback resistor and 10 kΩ resistor to a low-impedance reference has an ideal small-signal gain of 11 before frequency shaping or clipping is considered. This arithmetic helps check the schematic; it is not a complete overdrive design.

Guitar Effects PCB Layouts

Good guitar effects PCB layouts follow the audio path from input to output and keep high-gain feedback, clock signals and switching currents away from the input. Guitar pedal PCB design begins with placement that makes the quiet path short before routing starts.

  • Place the input buffer or first gain device close to the input connection.
  • Keep op-amp feedback components beside the relevant pins.
  • Separate the final high-level output from the low-level input to reduce unintended feedback.
  • Place local decoupling close to each IC supply connection.
  • Keep LED, relay and digital return currents out of sensitive analog reference paths.

A continuous ground reference is often easier to control than arbitrary ground splits. Do not route a sensitive signal across a gap in its return plane. Where multiple supply or signal domains exist, plan their current paths rather than relying on labels such as “analog ground” to solve coupling.

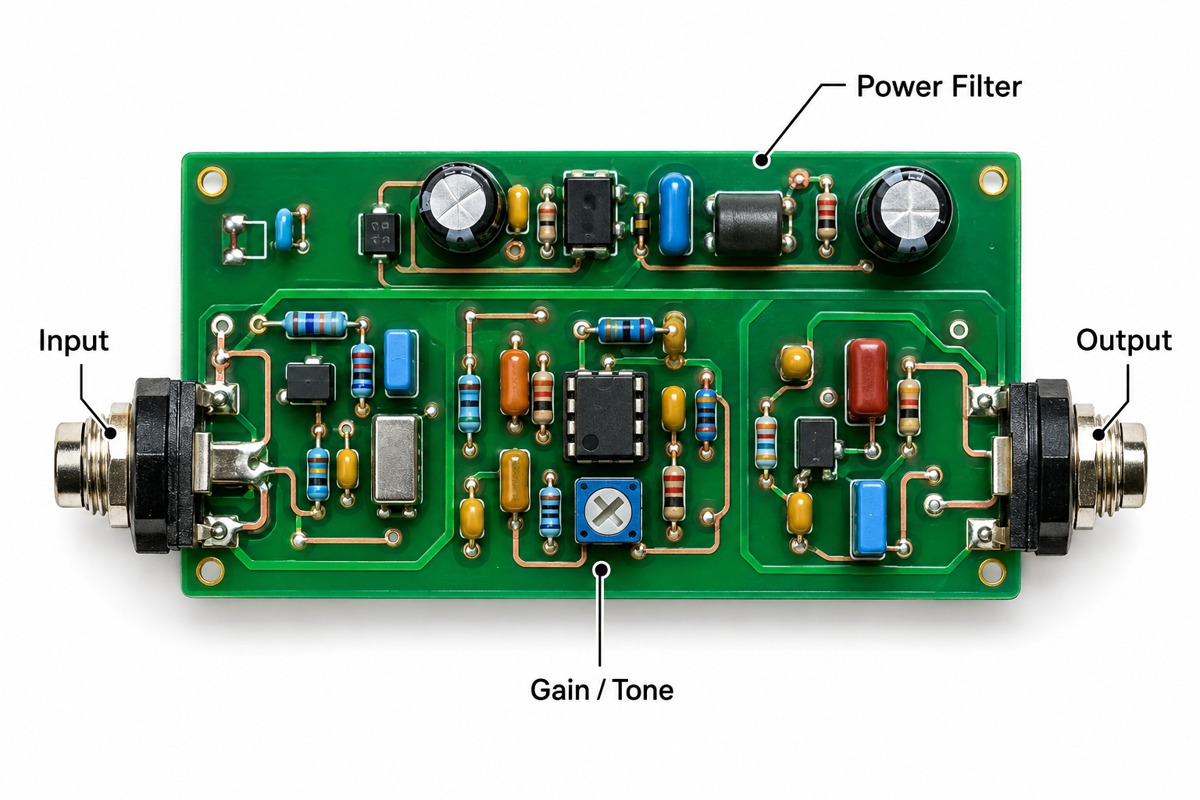
Guitar pedal PCB showing separated input, gain and tone, output and power filter areas

How Should a 9 V Pedal Supply Be Designed?

A 9 V pedal supply needs the correct connector polarity, protection, filtering and a bias reference compatible with the audio circuit. Many pedals use center-negative DC power, but the actual product specification must control the design.

For a single-supply analog circuit, a nominal 4.5 V reference may center the audio signal between ground and 9 V. That reference is not chassis ground. Its impedance and loading matter: shared bias movement can modulate multiple gain stages.

Check the exact amplifier variant. Texas Instruments lists a 7 V minimum total supply for the conventional TL072, while the TL072H has a different 4.5–40 V supply range. Similar names do not guarantee identical common-mode limits or output swing. A part operating on 9 V can still distort unintentionally if its inputs or outputs approach their limits.

A 100 nF ceramic capacitor near an IC supply is a common local-decoupling starting point, with bulk capacitance selected for the supply path. Confirm stability and transient behavior using the chosen device’s data sheet; do not copy capacitor values blindly.

Which PCB Construction Fits an Effects Pedal?

A two-layer FR-4 PCB is sufficient for many compact analog effects, while DSP pedals with dense digital routing may benefit from four or more layers. Layer count should follow routing, return-path and power-distribution needs.

Design item Example starting specification
Analog pedal construction 2-layer FR-4
Finished thickness 1.6 mm, subject to mechanical fit
Copper 1 oz nominal, subject to current and fabrication requirements
Through-hole IC example 8-pin DIP, typically 2.54 mm lead pitch
Surface-mount IC example SOIC-8, typically 1.27 mm lead pitch
Audio connector 6.35 mm jack type selected to match enclosure and footprint

These are design examples, not a fixed recipe or a list of manufacturing limits. Check the exact component drawing. Different jack bodies, potentiometer heights and switch footprints can make two electrically identical boards mechanically incompatible.

Should You Use Through-Hole or SMT Assembly?

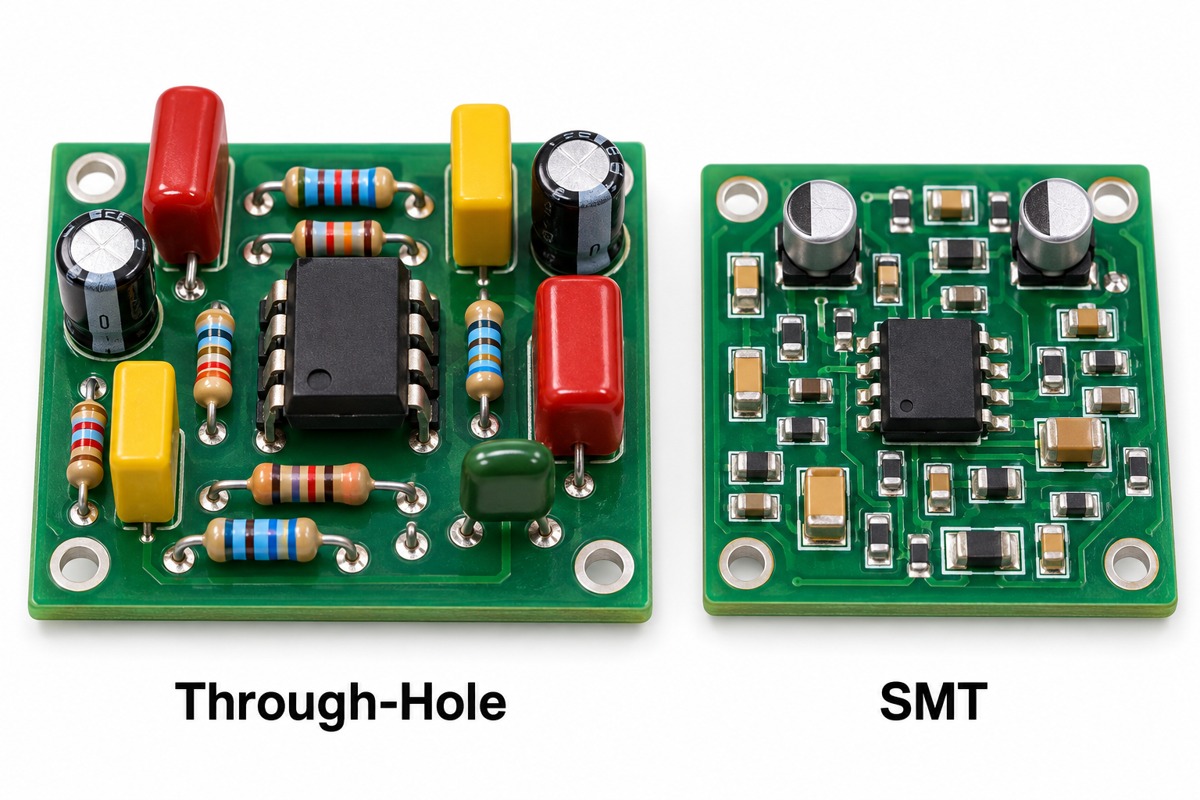
Through-hole parts are convenient for hand-built prototypes and modification; SMT reduces board area and supports automated placement. Mixed assembly often suits pedals that combine small audio electronics with large controls and connectors.

Neither method inherently produces a better tone. Compare the actual resistor tolerance, capacitor behavior, semiconductor characteristics and parasitics. A substitution that preserves a resistance value but changes a potentiometer taper or transistor pinout can still change the product.

For assembly release, specify manufacturer part numbers and approved alternatives. Mark electrolytic polarity, diode orientation and IC pin 1 clearly. Keep component bodies and solder joints away from mounting hardware and enclosure contact areas.

Through-hole and SMT guitar effects PCB assemblies compared side by side

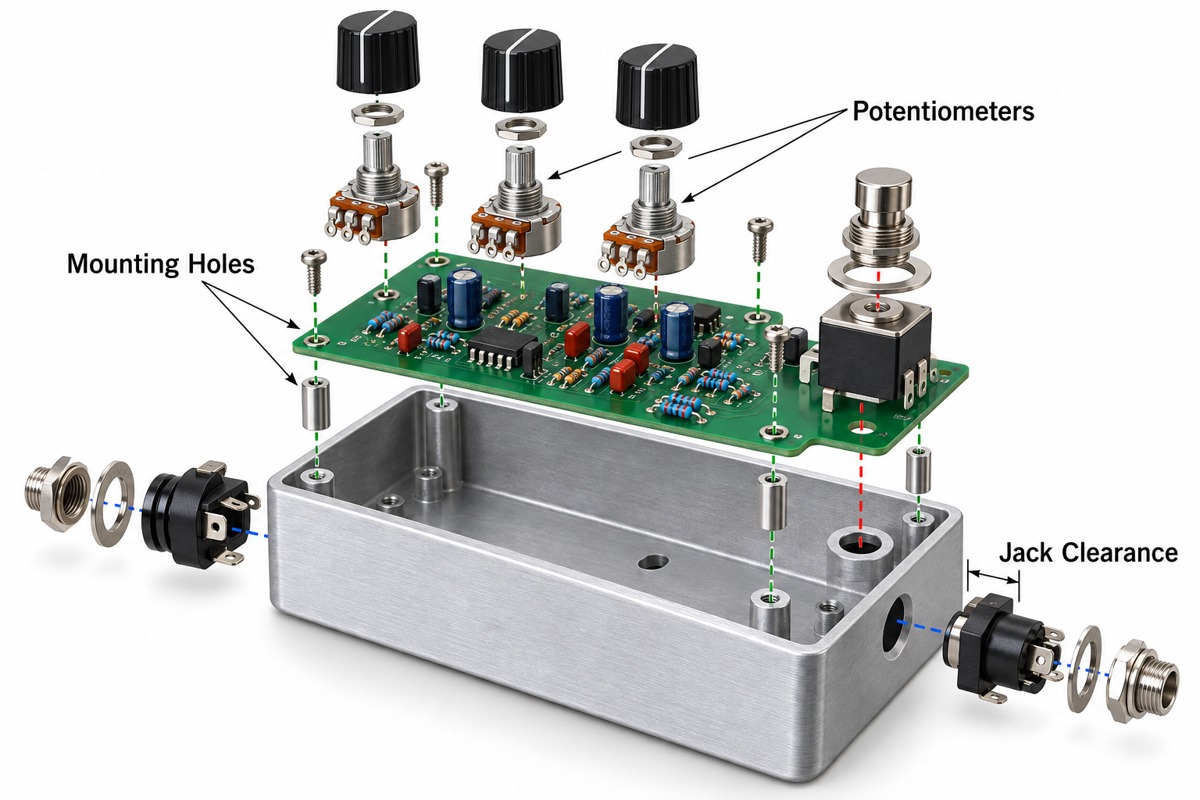
What Mechanical Checks Prevent Enclosure Problems?

Check the assembled board, control shafts, jacks, footswitch and lid together in a mechanical model or physical fit trial. The bare PCB outline alone cannot prove that a pedal will close without interference.

  • Match mounting-hole positions to the actual enclosure drawing.
  • Check component height against the lid and base, including tolerances.
  • Allow jack plugs, switch terminals and solder joints their full clearance.
  • Verify potentiometer shaft length, body height and knob seating.
  • Support heavy controls so repeated foot operation does not load small solder joints.

Plan insulation where the underside of the board can approach the metal enclosure. Connector shields and chassis connections should follow the grounding design, not accidental contact through a mounting screw.

Exploded guitar pedal showing PCB mounting holes, potentiometers and jack clearance

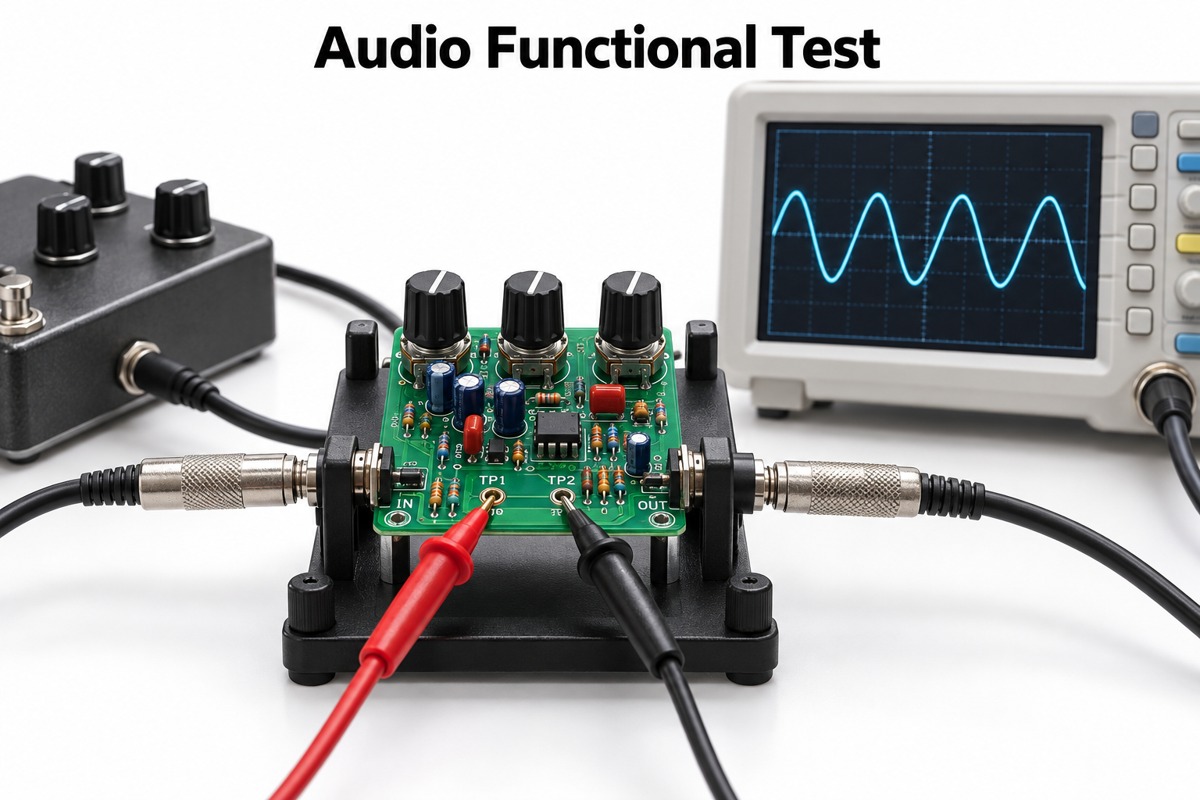
How Should a Guitar Effects PCB Be Tested?

Test supply current and DC bias first, then measure the audio path, controls, bypass and noise under defined input and output conditions. A continuity check alone cannot confirm an effects pedal’s sound or stability.

  1. Unpowered checks: inspect orientation, solder bridges, connector wiring and supply resistance.
  2. Current-limited power-up: compare current consumption and bias voltages with the design targets.
  3. Signal tracing: inject a known signal, such as a 1 kHz sine wave, and follow it through each stage.
  4. Functional sweep: verify gain, tone controls, clipping onset or delay behavior over the intended settings.
  5. Noise and switching: measure with a defined source termination, bandwidth and gain setting; check bypass pops and power-on behavior.
  6. Enclosed test: repeat the relevant checks in the final metal enclosure with the intended supply and cables.

Use a low input amplitude when measuring clean gain, then increase it deliberately to assess clipping. Record test levels and loading so the next batch can be compared with the approved reference unit. There is no universal pass/fail noise number for every pedal.

Audio functional testing of a populated guitar pedal PCB using a fixture and oscilloscope

Why Does a Pedal PCB Hum, Oscillate or Pop?

Hum usually points toward supply or grounding coupling; oscillation often comes from unintended feedback or unstable stages; switching pops can result from DC differences and charge redistribution. Diagnose the symptom before changing parts.

Symptom First checks
Hum or buzz Supply ripple, shield connection, loop area, input termination
High-pitched whine Clock or charge-pump coupling into the audio path
Oscillation at high gain Input/output proximity, feedback layout, capacitive loading
Pop during bypass DC at switch contacts, coupling-capacitor charging, switching sequence
No audio Power polarity, IC orientation, jack wiring, switch continuity

Use an oscilloscope where needed: an oscillating stage may sound weak or harsh rather than produce an obvious audible whistle. Compare one section at a time with the schematic and reference board.

FAQ About Guitar Effects PCB

Can a DIY guitar pedal PCB become a production product?

Yes, after the circuit rights, mechanical fit, BOM, manufacturing data and acceptance tests are resolved. A successful hand-built prototype does not by itself establish repeatability across substituted parts and production batches.

Does a gold finish improve pedal tone?

A surface finish should be selected for solderability, storage and any contact requirement. A claim that a gold PCB finish inherently improves the audio tone is not a substitute for measured circuit performance.

Does every pedal need a four-layer board?

No. Many analog pedals work well on two layers. More layers can help dense DSP layouts and return-path planning, but they do not correct a poor schematic or unsuitable power circuit.

Can one PCB support several effect versions?

Yes, with controlled option parts, jumpers or alternate population. Each version needs an identified BOM and a matching test configuration. Unused branches and long routing stubs should be assessed rather than left accidentally connected.

Are commercial pedal layouts free to copy?

Not necessarily. Publicly visible schematics or layout files can carry license restrictions. Confirm permission for the circuit files, artwork, firmware, trademarks and intended commercial use before sending them for manufacture.

How Can EBest Circuit Support Custom Pedal Manufacturing?

We support fabrication, component sourcing and assembly of customer-approved effects boards, with inspection and functional testing defined for the project. Our PCB design guidance also helps resolve manufacturing and mechanical issues before the design is released.

For a new pedal or a production transfer, contact sales@bestpcbs.com. Tell us whether you need bare boards or populated assemblies, and what audio and control tests define an acceptable unit. We can review the manufacturing scope without treating a generic continuity test as a finished audio test.

You may also like

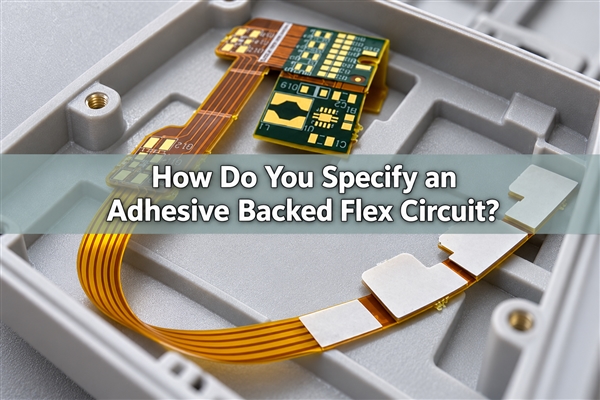
How Do You Specify an Adhesive Backed Flex Circuit?

October 29th, 2026

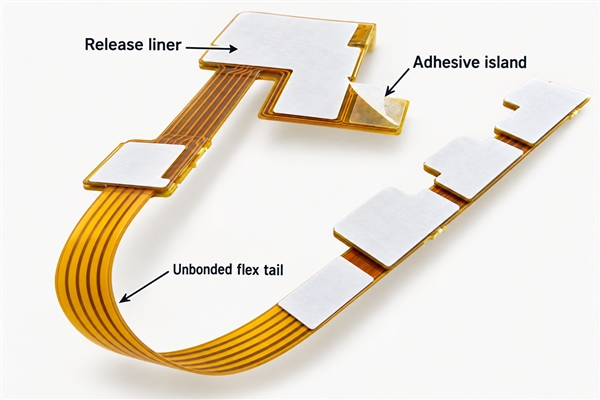
An adhesive backed flex circuit combines a flexible printed circuit with a mounting adhesive on selected areas of its rear surface. A removable liner protects the adhesive until installation. The result is a low-profile electrical interconnect that can be fixed inside a housing without adding a fastener at every mounting point. Reliable mounting depends on the housing surface, adhesive pattern, assembly temperature and loads at the free flex tail, not simply on choosing a tape that feels sticky.

Adhesive backed flex circuit with selective rear release liners in an enclosure

What Is an Adhesive Backed Flex Circuit?

An adhesive backed flex circuit is usually a finished flex PCB with a pressure-sensitive adhesive, or PSA, added for mechanical attachment. The copper traces carry the electrical signals; the backing holds designated regions in position. Removing the release liner exposes the adhesive for bonding to the specified surface.

The adhesive does not have to cover the whole board. Separate mounting islands can secure component areas while leaving a tail free to reach a connector. This is useful when a housing has limited room for clips, or when an interconnect must follow a fixed route between two boards. The mounting outline and the electrical circuit outline are therefore separate drawing features.

Is Adhesive Backing the Same as an Adhesive-Based Flex Core?

No. Adhesive backing sits outside the finished circuit for installation. An adhesive-based flex core uses an internal bonding layer between copper and the insulating film. Coverlay adhesive has another job: attaching the protective coverlay over the etched circuit.

An adhesiveless flex circuit can still have mounting adhesive on its back. “Adhesiveless” describes the core construction, not necessarily every layer added to the finished part. For an adhesive flex PCB quotation, send us a drawing that identifies whether the adhesive belongs in the core, under a stiffener or on the rear mounting surface. These locations require different constructions and production steps.

A bonded stiffener also does not turn a flex PCB into a rigid flex circuit. A rigid-flex board integrates electrically interconnected rigid and flexible sections. A stiffener attached to the back of a flex circuit primarily supplies mechanical support.

Which Adhesive Should You Use for a Flex Circuit?

Select the flex circuit adhesive against both mating surfaces and the required function. For ordinary mounting, a nonconductive acrylic PSA may be suitable, but adhesion to bare metal, painted metal and molded plastic can be very different. Specify the actual finish, including coatings or mold-release residues, rather than just writing “plastic enclosure.”

  • Mechanical retention: evaluate peel resistance, shear creep and edge lifting on the intended housing material.
  • Heat transfer: use a material with documented thermal properties and assess the complete heat path; ordinary mounting tape is not automatically a thermal interface material.
  • Electrical grounding: a conductive adhesive needs a designed exposed ground contact and a suitable mating conductor. Nonconductive PSA does not provide that connection.
  • Component support: compare a PSA-attached stiffener with a laminated stiffener against soldering temperature and mechanical loads.

A flexible circuit board adhesive that performs well in a room-temperature peel test may still creep under continuous heat and load. For a connector tail, the force direction matters as much as the adhesive area: a pull that peels one edge can be more demanding than a distributed in-plane load.

Which Adhesive Parameters Should Be on the Drawing?

The drawing should identify the adhesive grade, installed thickness, pattern, position tolerance, mating surface and exposure conditions. Material data also needs its test method and conditioning time. Without those details, two numerical peel-strength values are not directly comparable.

ParameterExample or required entryHow to use it
Adhesive thickness3M 467MP: 0.06 mm; 468MP: 0.13 mm in the cited family dataIdentify the exact grade and datasheet revision; these are material examples, not a mandatory flex stack-up.
Release liner467MP example: 0.11 mm polycoated kraft linerInclude it in delivery/handling thickness, but exclude it from the installed assembly after removal.
90-degree peel adhesion467MP: 10 N/cm on stainless steel after 72 hours at room temperatureTypical ASTM D3330 result with aluminum-foil backing; not a finished-flex acceptance limit.
PSA outline and cutoutsDimensioned drawing in mm, referenced to board datumsDefine edge setback, holes, exposed pads and no-adhesive areas.
Position toleranceAgreed bilateral or profile tolerance in mmCheck combined flex-outline, adhesive-cut and placement variation.
Thermal exposureOperating temperature, peak process temperature, duration and number of cyclesSeparate service exposure from soldering and rework.
Bond qualificationPeel angle/rate, dwell, surface preparation, load, environment and acceptance limitsUse repeatable tests on the actual bonded materials.

The numerical material examples above come from the 3M 467MP technical data sheet, May 2017. They describe typical material properties under stated conditions, not our finished-board test results. The ordered grade and current approved specification govern production.

Keep the installed thickness calculation separate from shipping thickness. For example, an assumed 0.15 mm finished flex plus 0.06 mm adhesive gives 0.21 mm before compression and tolerances. Adding a 0.11 mm removable liner gives 0.32 mm as delivered. This arithmetic example is not a recommended circuit thickness; components, stiffeners and their tolerances must be added wherever present.

Where Should Adhesive Be Placed on a Flexible PCB?

Place adhesive where the circuit must remain fixed, and keep the intended moving or installation-bend region free unless the design specifically qualifies a bonded fold. Do not run a backing layer across connector contacts, test pads or openings that must remain accessible.
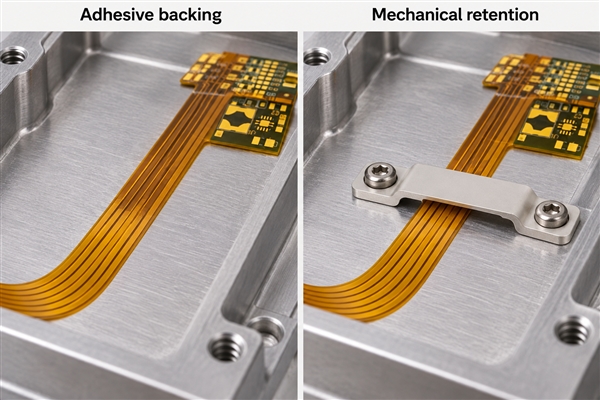
Selective adhesive islands and release liners with an unbonded flexible tail

Dimension each adhesive island from a defined board datum. A drawing should also show the mounting side, orientation and exclusion zones. Small disconnected patches can be difficult to handle and align, so the smallest feature must be reviewed together with the intended cutting and placement process rather than assigned a universal minimum size.

At the end of a bonded region, avoid forcing the free tail around a sharp enclosure edge. Provide a smooth transition and a supported routing path. If the tail plugs into a connector on an FR4 PCB, set its installed position from the connector location and insertion direction, not only from the housing wall. Adhesive should retain the route without preloading the connector.

How Do Release Liners Affect Flex Circuit Assembly?

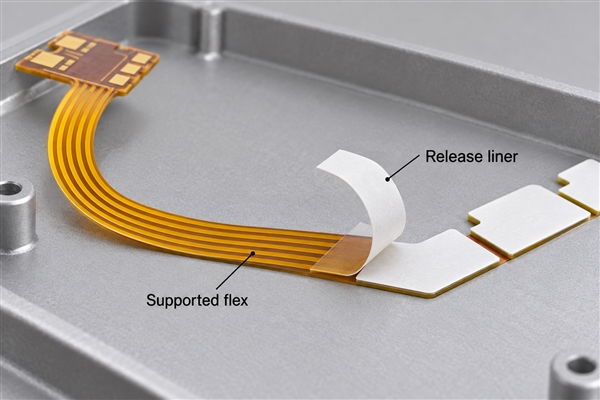
The liner determines how easily an operator can expose and position the adhesive without damaging the flex. A fully flush liner can be difficult to start, especially beside a narrow tail. A pull tab or split liner can provide a controlled gripping point while keeping the adhesive protected.
Specify which region is peeled first and whether the part is located by a fixture, a housing feature or a visual reference. The operator should be able to position the circuit before applying final bonding pressure. A liner tab must remain accessible at that stage; a tab trapped under the circuit or a nearby component defeats its purpose.
Check liner removal during prototype assembly, not just on a flat drawing. If the flex bends sharply when the liner is pulled, support the circuit close to the peel front. Avoid using a connector tail or a populated area as the handle.

Can Adhesive-Backed Flex Circuits Go Through Reflow?

Only when the exact adhesive and liner system is qualified for the complete thermal profile. A short-term heat-resistance value alone does not establish compatibility with reflow, repeated soldering or subsequent cleaning.

One practical route is to assemble and clean the circuit first, then apply the mounting PSA. Another is to use a verified assembly-compatible adhesive before soldering. The correct sequence depends on access to the rear surface, support tooling and the approved material. Do not infer reflow suitability from the polyimide substrate rating; the adhesive or liner can be the limiting layer.

For our PCB assembly service, we support SMT, through-hole and mixed assembly, with capabilities down to 01005 components and 0.25 mm BGA pitch on suitable projects. Flex handling, support fixtures and adhesive processing still need project-specific review. Include the adhesive operation in the assembly drawing and BOM so it is not treated as an unspecified step after soldering.

How Do You Install a Peel-and-Stick Flex Circuit?

Supported flex circuit with its release liner being peeled before installation

Install the circuit on a clean, dry and compatible surface, locate it without stretching the tail, and apply controlled pressure to the intended bonded areas. The adhesive manufacturer’s preparation, temperature and dwell instructions should become part of the assembly procedure.

  1. Inspect the receiving surface. Check for oil, dust, loose coating, rough edges and geometry that prevents contact. Confirm that the specified cleaning method is compatible with both materials.
  2. Dry-fit with the liner in place. Verify connector reach, bend position, component clearance and access to liner tabs.
  3. Expose the intended adhesive region. Handle the liner, not the adhesive, and support the flex as the liner is removed.
  4. Locate and bond progressively. Use the agreed datum or fixture. Avoid trapping wrinkles or stretching the circuit to meet a misplaced reference.
  5. Apply pressure with appropriate support. Support the opposite side; do not press directly on fragile components or unsupported tails.
  6. Allow the specified dwell and inspect. Confirm alignment, edge contact and electrical continuity before applying the full service load.

Record the installation conditions when a prototype fails. Repeating a test with a freshly cleaned housing, a different dwell time and a different peel direction creates a different test, not a direct repeat of the first result.

Adhesive Backing vs Mechanical Mounting: Which Should You Choose?

Adhesive-backed flex mounting compared with a mechanical retaining bridge

Adhesive backing suits low-profile retention over a defined surface. Mechanical mounting is often preferable where disassembly, concentrated loads or positive location dominate. A hybrid design can use adhesive to keep a flex route flat and a separate feature to carry connector or cable loads.

Design needAdhesive backingClips, clamps or fasteners
Limited heightThin bond line with no fastener head in the bonded regionNeeds space for the retaining feature and assembly access
Repeated servicingRemoval can damage the flex or leave residue; replacement may be neededCan provide a planned release mechanism
Continuous pull or heatRequires creep testing for the actual area and load directionCan transfer load into a designed structural feature
Surface variationSensitive to contamination, texture and coating adhesionLess dependent on surface chemistry, but fit and clamp pressure matter
Moving tailRetain stationary regions, leaving a controlled free transitionProvide strain relief without pinching or creating a sharp bend

A thicker adhesive is not automatically a substitute for a clamp. Likewise, adding a screw near a thin flex does not automatically make the assembly stronger: local pressure, hole support and trace clearance need a designed load path.

What Causes Adhesive-Backed Flex Circuits to Lift or Slip?

Lifting usually indicates a local separation or peel load, while slipping suggests movement within the bond or at an interface. Similar-looking failures can have different causes. Preserve the failed surfaces and compare the result with the installation record before changing the adhesive grade.

Observed conditionWhat to checkUseful next step
One edge lifts after the tail is connectedTail preload, connector position, abrupt bend at the bonded edgeTest the same bond with the tail unloaded, then correct routing or strain relief
Patch shifts during hot dwellShear load, temperature, bonded area and adhesive creepRepeat with recorded load and displacement over time
Adhesive releases from a painted housingAdhesive-to-paint interface versus paint-to-housing separationInspect both faces; qualify the actual coating system
Wrinkle or unbonded pocketPlacement sequence, flatness, local particles and support toolingReview the installation method and contact pattern
Electrical failure after repositioningCreased copper, torn coverlay or stressed jointsInspect the circuit and test continuity; stronger tape will not repair trace damage

How Should You Test an Adhesive-Backed Flex Circuit?

Test mechanical retention and electrical function separately, then combine them under the intended environment. A continuity pass does not prove the bond is stable, and a strong peel result does not prove the copper survived installation.

  • Peel: fix the angle, rate, sample width, dwell and substrate. Report force per width and where separation occurred.
  • Static shear: define bonded area, applied load, orientation, temperature and duration. Record movement or time to failure.
  • Environmental exposure: use the specified heat, humidity or chemical conditions, then repeat the relevant retention and electrical checks.
  • Installation trial: evaluate liner handling, alignment, wrinkles and connector loading using the actual enclosure or a representative fixture.
  • Electrical checks: compare continuity and insulation results before and after installation and environmental exposure, using the approved circuit test requirements.

Test coupons are useful for isolating material behavior, but a flat strip does not reproduce every stress in a populated flex assembly. Include the real adhesive boundary, tail routing and housing finish in final qualification. Agree acceptance limits before testing rather than choosing them after the results are known.

What Files Are Needed for an Adhesive-Backed Flex PCB Quote?

Send the circuit fabrication data together with a separate, dimensioned adhesive drawing. At EBest Circuit (Best Technology), we provide flexible and rigid-flex PCB manufacturing and assembly support. The quotation needs to distinguish the electrical board, mounting adhesive, liner and any post-assembly application work.

  • Gerber or other accepted fabrication files, drill data and the required flex stack-up.
  • Adhesive grade or functional requirements, with any approved-alternative restrictions.
  • Adhesive side, outline, openings, placement datums and tolerances.
  • Liner material, pull tabs, split positions and removal sequence.
  • Housing material and finish, installed geometry, load direction and operating environment.
  • BOM and assembly files for populated parts, plus soldering, cleaning and adhesive-application sequence.
  • Prototype and production quantities, inspection requirements and packaging expectations.

Email sales@bestpcbs.com with the drawing and intended mounting surface. We can review the fabrication and assembly requirements together, identify unresolved adhesive details before quoting, and define what the delivered circuit includes. A tape part number without its placement and process requirements is not a complete manufacturing specification.

Adhesive Backed Flex Circuit FAQs

1. Is flex circuit tape electrically conductive?

Not necessarily. Flex circuit tape can mean ordinary mounting PSA, insulating tape or a specialized conductive product. For grounding, specify conductivity direction, exposed contact geometry and resistance requirements; do not rely on the word “tape.”

2. Can you remove and reuse an adhesive-backed circuit?

Do not assume reuse is acceptable. Removal may distort the circuit or contaminate the adhesive. A serviceable design needs a defined release method and replacement criteria, including electrical checks if the circuit is retained.

3. Does adhesive backing make a flex circuit waterproof?

No. A mounting bond alone does not establish an enclosure ingress rating. Edges, connectors, holes and material interfaces still need a sealing design and appropriate testing.

4. Does an adhesive circuit replace soldered connections?

A mechanically mounted adhesive circuit still needs its specified electrical termination. Backing adhesive normally holds the board in position; it does not replace connector contacts or solder joints. Conductive bonding is a separate interconnection design.

You may also like

G10 Material: Properties, Uses and G10 vs FR-4

October 29th, 2026

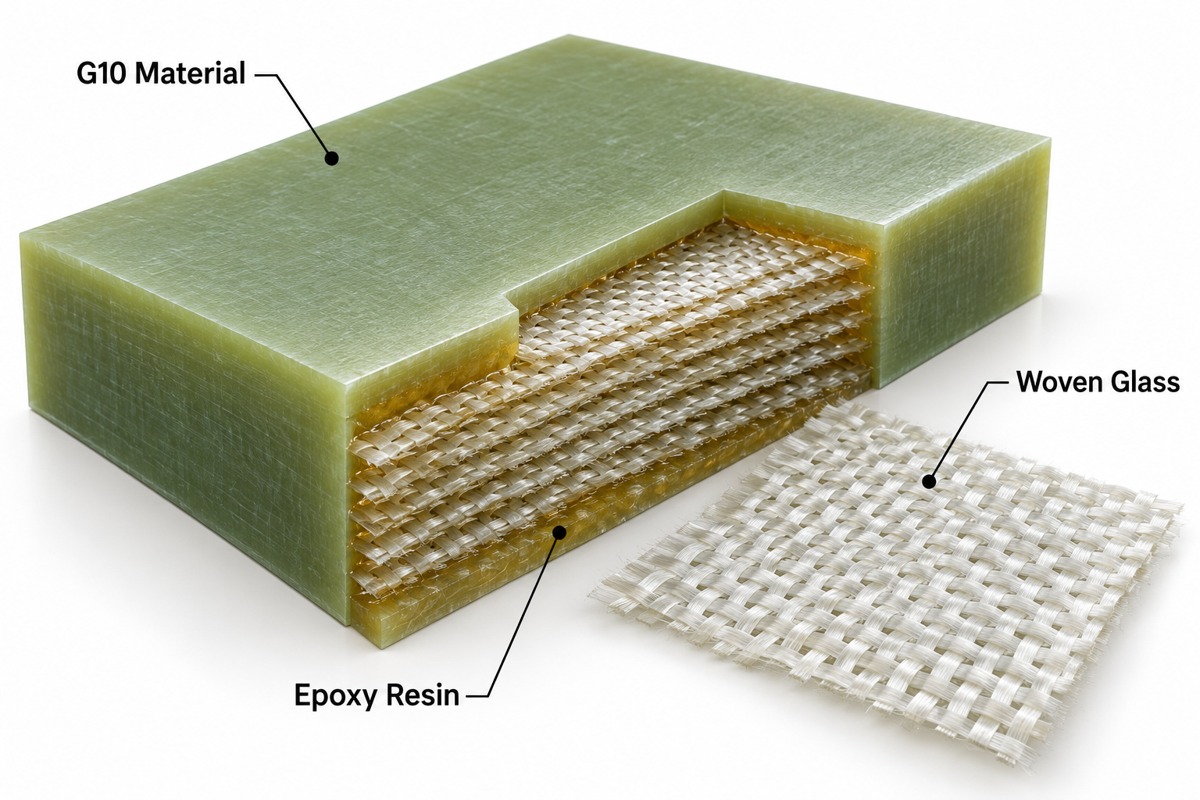
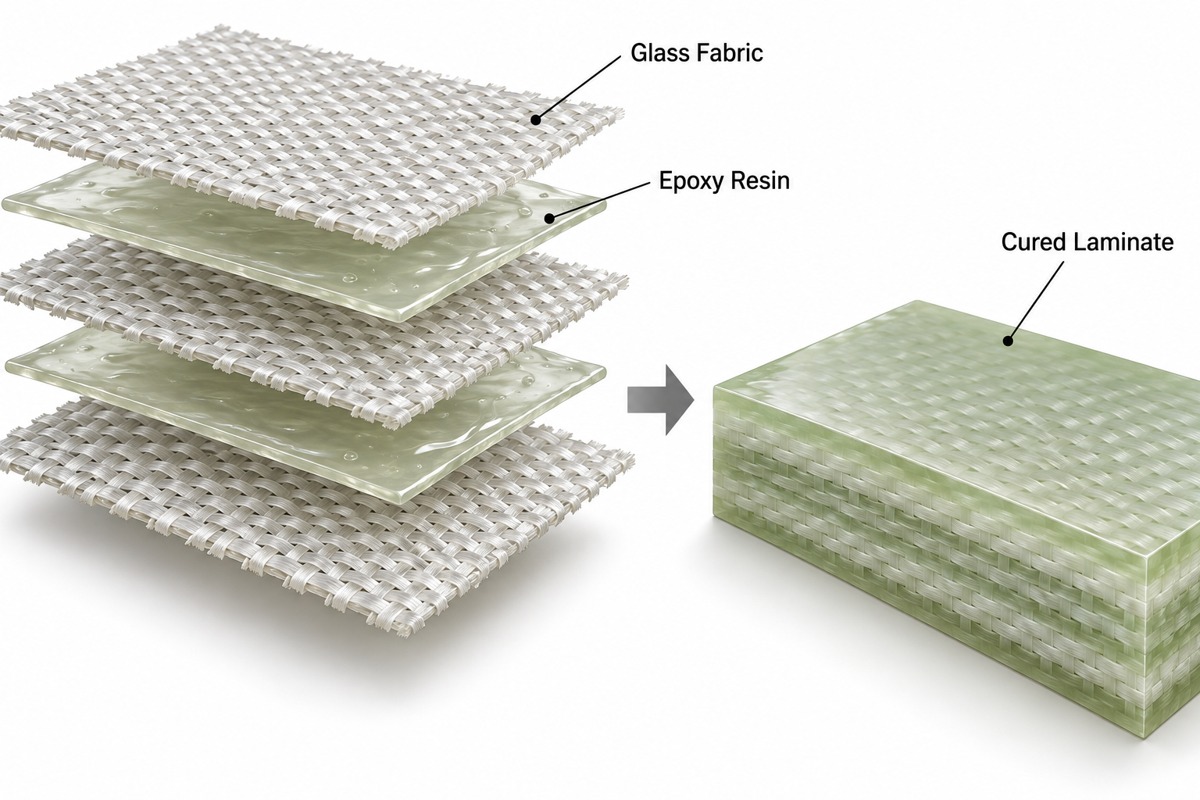
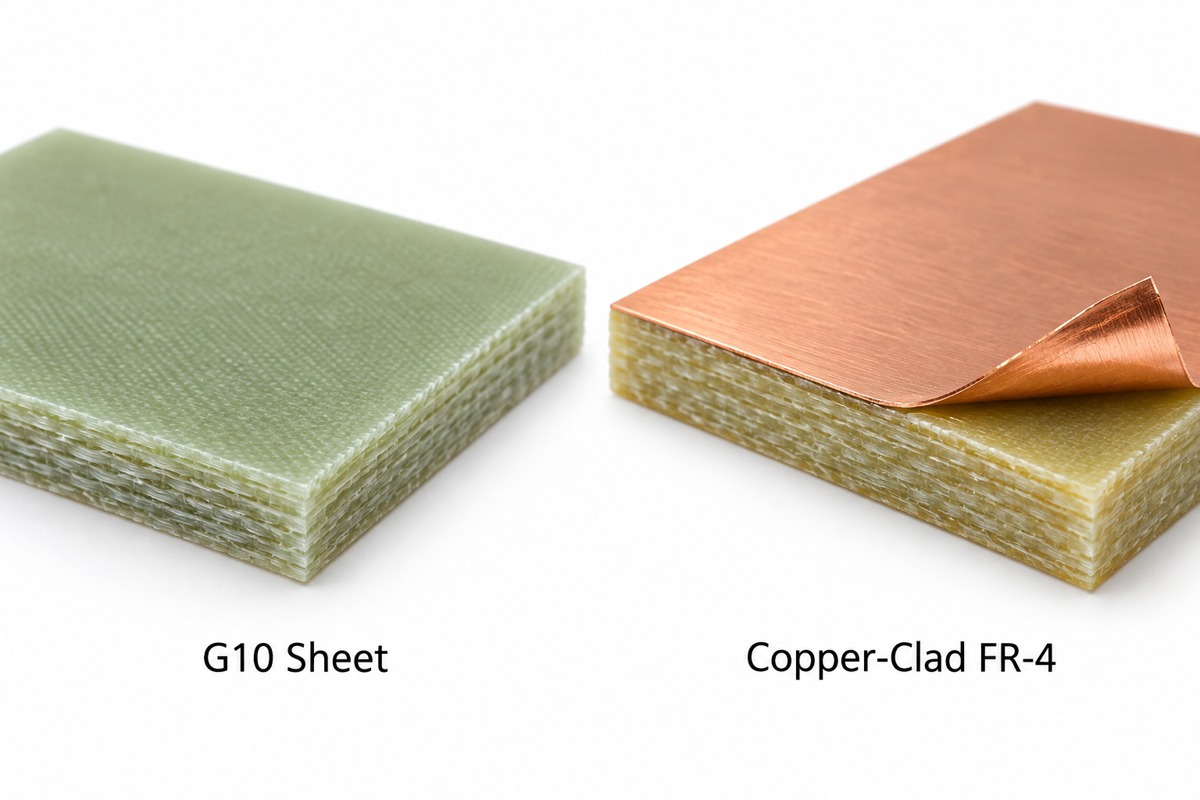
g10 material is a rigid electrical-insulating composite made from woven glass fabric bonded with cured epoxy resin under heat and pressure. It combines structural strength, low moisture absorption and electrical insulation, making it useful for spacers, terminal supports, backing plates and other machined parts. G10 and FR-4 share a glass–epoxy construction, but G10 alone does not establish the flame-retardant performance associated with FR-4. A plain G10 sheet is also not the same product as copper-clad PCB laminate.

At EBest Circuit, we help customers translate electrical, thermal and mechanical requirements into manufacturable circuit boards. For a circuit-board project, our FR-4 PCB manufacturing review starts with the specified laminate grade, stackup and copper requirements—not simply a green sheet described as “G10.”

G10 glass epoxy laminate cutaway showing woven glass and cured epoxy

Key Takeaways

  • G10 is a woven-glass-reinforced epoxy thermoset, not a metal or an unreinforced plastic.
  • The material provides both electrical insulation and mechanical support; its properties depend on the specific grade, direction and test conditions.
  • G10 and FR-4 are not interchangeable flame-rating specifications. Some commercial products are qualified and sold as G10/FR-4.
  • Service temperature, glass-transition temperature and soldering exposure describe different limits.
  • Glass reinforcement makes machining abrasive; tool selection, edge support and dust control matter.
  • For PCB fabrication, specify copper-clad laminate, finished thickness, copper weight and the required material qualification.

What Is G10 Material Made Of?

G10 consists of continuous woven glass cloth and an epoxy resin system that cures into a rigid thermoset matrix. The glass carries much of the mechanical load; the resin bonds the layers and insulates them.

Manufacture generally involves impregnating glass cloth with resin, stacking the required plies, and consolidating the stack under controlled heat and pressure. After curing, the panel can be cut or machined. It does not melt and flow again like a thermoplastic.

Pigments, resin formulation, cloth construction and processing can vary between products. Color does not identify a grade or prove electrical performance.

Woven fiberglass plies and epoxy consolidated into a rigid G10 laminate

G10 Material Properties

G10 material properties include high stiffness, electrical insulation and moisture resistance, but numerical values must come from the selected product’s data sheet. Mechanical direction and electrical test frequency can change the result.

For a concrete reference, Attwater’s EPGC201 product, described as closest to NEMA G10, lists the following typical values. These are one supplier’s material data, not EBest Circuit production limits or universal G10 specifications.

Property Published typical value
Density 2 g/cm³
Flexural strength 485 MPa
Relative permittivity at 1 MHz 5.2
Dissipation factor at 1 MHz 0.025
Electric strength, flat rapid test 15 kV/mm
Continuous thermal rating 130°C
Intermittent thermal rating 140°C

Do not multiply electric strength by the part thickness to set a finished assembly’s working voltage. Creepage, clearance, humidity, surface contamination, edges and the applicable equipment standard still govern insulation design.

How Is G10 Different from FR-4?

The main distinction is that FR-4 specifies a flame-retardant glass–epoxy grade, while the name G10 by itself does not establish that flame performance. Their shared construction explains why suppliers sometimes list a dual-qualified “G10/FR-4” product.

Feature G10 FR-4
Reinforcement and binder Woven glass and epoxy Woven glass and flame-retardant epoxy system
Typical purchase form Insulating sheet, machined stock, rod or tube Unclad insulation stock or copper-clad PCB laminate
Fire-performance selection Do not infer a rating from the name alone Verify the exact grade, listing and thickness
PCB procurement Generic sheet designation is insufficient Specify an actual laminate and stackup

For example, Acculam Epoxyglas G10/FR4 is explicitly described as flame-retardant and qualified to NEMA FR4 and MIL-I-24768/27. That statement applies to the named product; it does not make every G10 sheet flame-retardant.

Unclad G10 insulating sheet compared with copper-clad FR-4 laminate

What Is the G10 Material Temperature Range?

The usable G10 material temperature range depends on the resin formulation, exposure time and required retained properties; it is not one universal minimum-to-maximum range. The EPGC201 example above lists 130°C continuous and 140°C intermittent ratings.

Those ratings are not the same as Tg, the glass-transition temperature, and they do not authorize an arbitrary solder-reflow profile. A short manufacturing excursion and years of service impose different stresses. For a PCB, check the laminate’s Tg, decomposition behavior, expansion and assembly suitability separately.

For cold environments, also check thermal contraction, fastener loads and thermal cycling. A material used in one cryogenic insulation design is not automatically qualified for another assembly.

Where Is G10 Used?

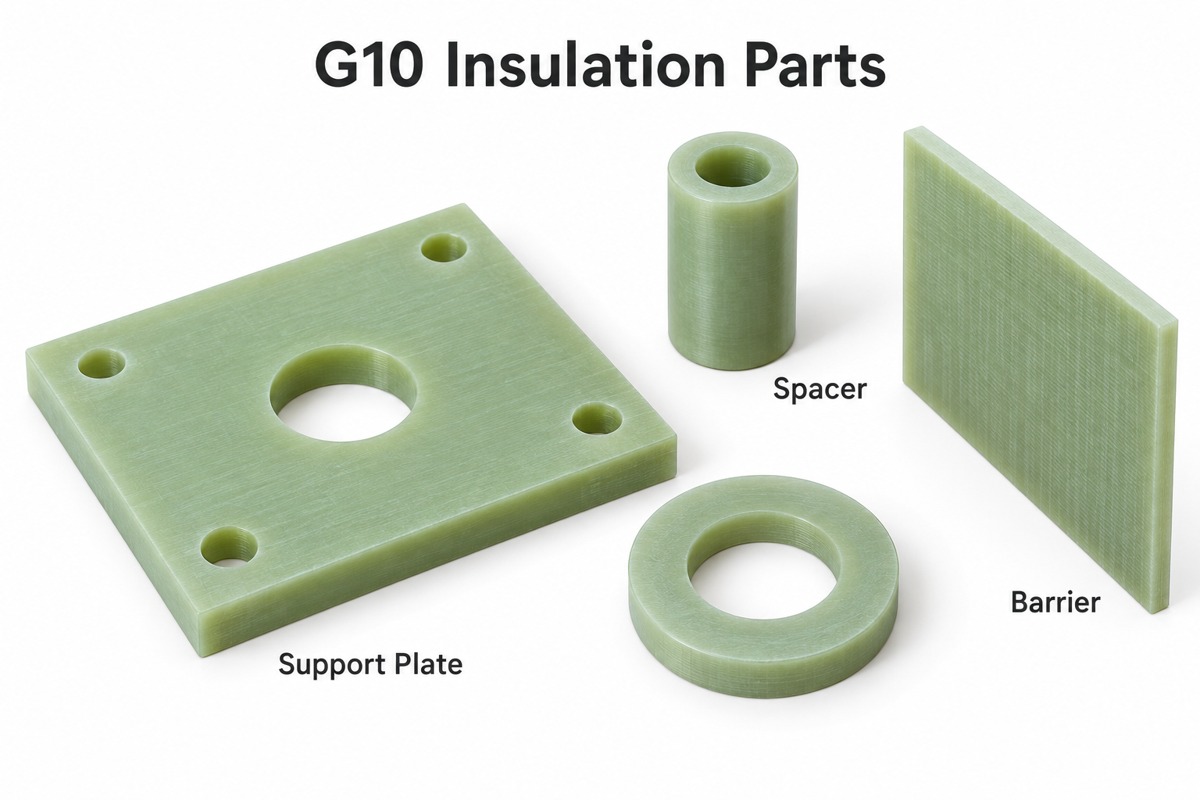
G10 is used where a part must support a load without creating an electrical conduction path, including terminal supports, insulating spacers, coil supports and phase barriers.

  • Electrical equipment: barriers, bushes, washers and terminal mounting plates.
  • Mechanical assemblies: nonmetallic support plates, fixtures and brackets.
  • Marine equipment: backing plates where strength and moisture resistance are useful.
  • Consumer products: textured knife-handle scales and similar grip components.

The grip of a knife scale depends on its texture and shape, not just the G10 name. Likewise, a marine backing plate still needs appropriate sealing, fastener design and load assessment. These applications do not establish suitability for food contact or another regulated use.

G10 insulation spacer, barrier and support plate on a white background

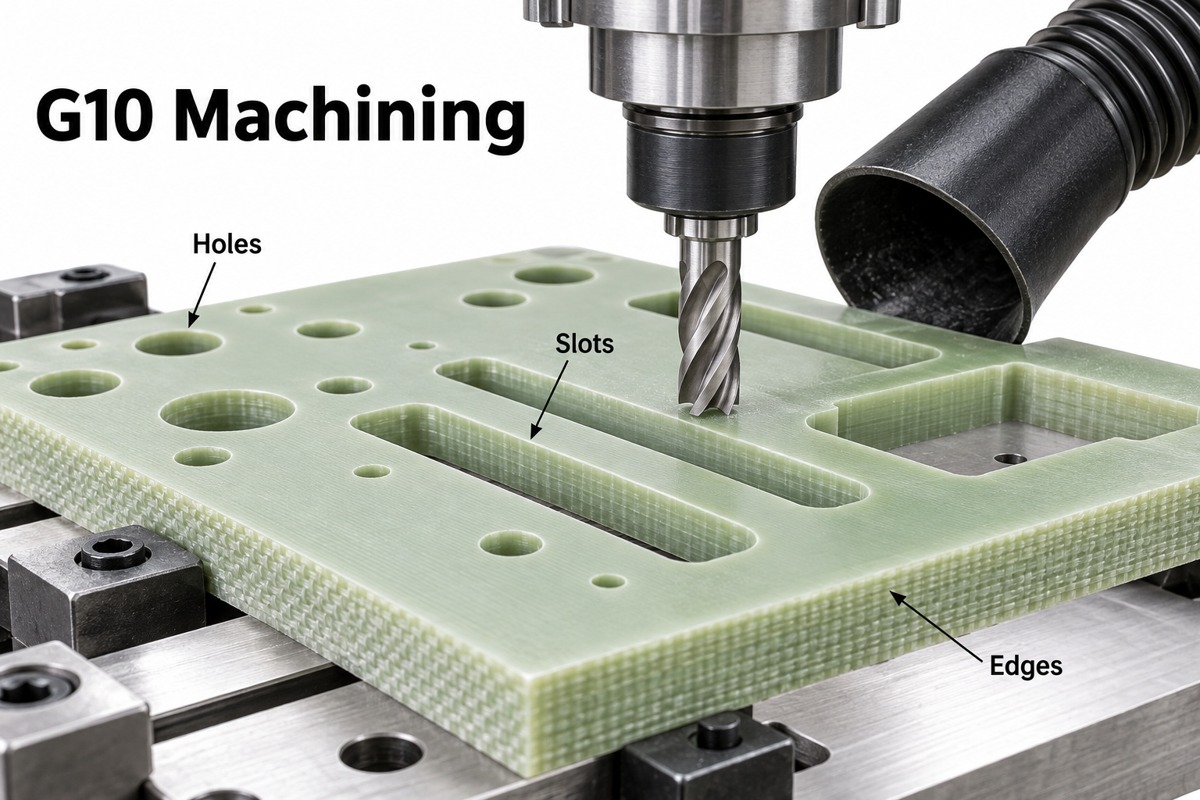
How to Cut G10 Material

G10 is commonly cut and drilled with tooling suitable for abrasive glass-reinforced composites, with support near the cut and effective dust extraction. Carbide tooling is a common choice; the tool supplier’s recommendations should set cutting conditions.

Use these machining controls:

  • Clamp the sheet securely and use sacrificial backing where needed to limit breakout.
  • Choose a cutter and feed that cut the fibers instead of rubbing and overheating the resin.
  • Inspect hole exits and routed edges for fraying, chipping and interlayer separation.
  • Use extraction and protective measures specified by the material safety data sheet and workplace assessment.

Do not treat glass–epoxy dust as ordinary harmless shop debris. Avoid uncontrolled dry sanding, and do not assume laser cutting is suitable: resin damage, fumes and edge quality require process-specific assessment.

Machining holes and slots in a G10 plate with a nearby extraction nozzle

Can a G10 Sheet Be Used as a PCB Substrate?

Glass–epoxy can form a PCB’s dielectric structure, but an ordinary unclad G10 sheet is not a drop-in replacement for a qualified copper-clad PCB laminate. It has no ready-made copper circuitry and may lack the required material qualification.

For a manufactured circuit board, define:

  • The laminate manufacturer, grade and required qualification.
  • Finished board thickness and tolerance—for example, a specified 1.6 mm board rather than unspecified sheet stock.
  • Copper weight, layer arrangement and dielectric thicknesses.
  • Flammability requirements and the assembly temperature exposure.
  • Electrical requirements, including impedance or high-frequency loss where relevant.

A 1 MHz dielectric value from an insulation-sheet data sheet is not sufficient to design a high-speed channel. Our PCB design review connects the material selection to routing, stackup and fabrication requirements. Assembly requirements must also be compatible with the chosen laminate.

What Changes the Cost of G10 Parts?

G10 part cost is driven by stock thickness, material utilization, machining time, tool wear and inspection requirements—not only the sheet’s unit price.

A flat rectangular spacer with two holes usually needs less machining than a thin part with deep pockets and closely toleranced slots. Surface finish, edge quality, batch quantity and certification documentation can also change the purchase price. Compare quotations for the same grade, dimensions and machining scope; generic “G10 price” listings may describe very different products.

FAQ About G10 Material

Is G10 the same as Garolite?

Garolite is a trade name used for several laminate grades. G10 identifies a particular glass–epoxy material class; “Garolite” alone does not tell you the resin, reinforcement or flame performance.

Is G10 electrically conductive?

Standard glass–epoxy G10 is an electrical insulator. Surface contamination, moisture, damaged edges or added conductive coatings can change an actual part’s behavior. Do not confuse glass reinforcement with conductive carbon fiber.

Is G10 waterproof?

G10 has low water absorption, not guaranteed zero absorption. For immersed or humid service, use the selected grade’s conditioned electrical and mechanical data and assess exposed edges and fastener penetrations.

Does G10 melt?

Cured G10 is a thermoset and does not remelt like a thermoplastic. Excess heat can still reduce stiffness, damage the resin and eventually cause decomposition. “Does not melt” does not mean unlimited heat resistance.

Is G10 stronger than aluminum?

There is no useful universal yes-or-no comparison. Tensile, flexural and compressive performance differ, and G10 is directional. Compare the actual laminate and aluminum alloy under the same loading, thickness and environmental conditions.

Can black G10 be identified by color alone?

No. Black pigment does not establish the laminate grade, fire rating or electrical properties. Use the product designation, data sheet and material documentation rather than appearance.

How Can EBest Circuit Support Your Glass–Epoxy PCB Project?

We support PCB fabrication and PCB assembly projects that need the right laminate, manufacturable stackup and compatible assembly process. If a drawing currently says only “G10,” we can review what the circuit board actually needs before fabrication.

Contact our engineering team at sales@bestpcbs.com with your design and operating requirements. We will help clarify the PCB material specification rather than assume that generic insulating stock meets it.

You may also like

ESP32 Pinout: GPIO, Power and Interface Pin Guide

October 23rd, 2026

The esp32 pinout identifies a board’s power, ground, control and GPIO connections. On a classic ESP32-WROOM development board, GPIO21 and GPIO22 are common I2C choices, GPIO1 and GPIO3 serve UART0, and GPIO34–39 are input-only at chip level. These are 3.3 V logic connections, not 5 V-tolerant inputs. The physical header arrangement depends on the board: a 30-pin DevKit-style board is not interchangeable with a 38-pin ESP32-DevKitC V4. This guide uses the classic ESP32-WROOM/DevKitC family as its reference and separates it from ESP32-S3 and ESP32-C3, which require different pin maps.

ESP32-DevKitC V4 WROOM structural overview showing both 19-pin headers, antenna and Micro-USB orientation

Key Takeaways

  • Match the exact chip, module and board revision before connecting wires or creating a PCB footprint.
  • GPIO numbers identify signals; they are not module-pad numbers or header-position numbers.
  • Classic WROOM boards reserve GPIO6–11 for flash. GPIO34–39 cannot drive outputs or provide internal pull-up/down resistors.
  • GPIO0, 2, 5, 12 and 15 are classic ESP32 strapping pins. External circuits must not impose incorrect levels during reset.
  • Use ADC1 inputs for analog measurements that must coexist with Wi-Fi on the classic ESP32.
  • I2C, SPI and UART assignments depend on firmware and board configuration; example pin choices are not universal hardware requirements.
  • A custom PCB also needs a stable supply, antenna clearance, programming access and functional testing—not just a copied pinout.

Which ESP32 Pinout Diagram Matches Your Board?

The correct ESP32 pinout diagram matches the module marking, development-board model and PCB revision—not just the word “ESP32” or the number of header pins.

Hardware you have Reference to use What changes
ESP32-WROOM module Exact module datasheet and land pattern Module pads, ground pad and antenna area
ESP32-DevKitC V4 with WROOM DevKitC V4 schematic and J2/J3 header tables 38 header positions, USB bridge and regulator
30-pin DevKit-style board That board manufacturer’s drawing Header order, omitted signals and power labels
ESP32-WROVER development board WROVER module plus board schematic PSRAM reserves GPIO16 and GPIO17
ESP32-S3 or ESP32-C3 board Matching S3/C3 module and board documentation GPIO map, USB functions, memory allocation and boot pins

Count pins on both sides, read the metal-shield marking, and compare the silkscreen beside the connector. A USB-C socket alone does not identify the chip family. If you are still choosing a development platform, our ESP32 vs Arduino comparison covers that separate decision.

At EBest Circuit, we support custom PCB fabrication and assembly. When a development-board prototype moves into a product, our PCB design and manufacturing review should work from the selected module’s documentation and the released schematic, not a generic internet pin diagram.

How Do GPIO Numbers Differ from Physical Pin Numbers?

A GPIO number identifies an ESP32 signal, while a physical pin number identifies its position on a particular chip, module or connector.

For example, GPIO21 is connected to position 6 on the DevKitC V4 J3 header. That does not make it “pin 6” in firmware. Code that selects GPIO21 must use the GPIO identifier expected by the software framework.

Complete 38-pin ESP32-DevKitC V4 WROOM pin map with J2 and J3 connector positions, GPIO labels and restricted pins
  • Chip pin: a terminal on the ESP32 IC package.
  • Module pad: a solder connection on the WROOM module.
  • Header position: a connector contact on a development board.

Keep GPIO net names consistent between the schematic and firmware. For a custom carrier board, also check the viewing direction: a bottom-view drawing can reverse the apparent left/right order.

ESP32 Pinout Reference

For a classic WROOM-based board, GPIO18, 19, 21, 22, 23, 25, 26, 27, 32 and 33 are useful starting choices for general digital I/O, provided the board has not already assigned them to another circuit.

Function Classic ESP32 GPIOs Selection rule
General digital I/O 18, 19, 21, 22, 23, 25, 26, 27, 32, 33 Check peripheral conflicts and connected hardware
Additional digital I/O 4, 13, 14, 16, 17 13/14 can serve JTAG; 16/17 depend on module memory use
Input-only GPIOs 34–39 at chip level No output drive or internal pull-up/down; 37/38 are not exposed on the DevKitC reference headers
Boot strapping 0, 2, 5, 12, 15 Check external pull resistors and reset-time levels
Flash interface 6–11 on WROOM Do not assign to external peripherals
UART0 TX: 1; RX: 3 Normally used by the programming/debug connection
ADC1 exposed on DevKitC 32, 33, 34, 35, 36, 39 Preferred for analog sensing while Wi-Fi operates
DAC outputs 25, 26 Classic ESP32 only; do not assume every ESP32-family chip has these DACs

“General I/O” does not mean every pin is suitable for every job. A pin used by an SPI display cannot simultaneously serve an unrelated sensor, and a GPIO should not directly power a relay or motor. Use an appropriate driver circuit for the load.

How Do 30-Pin and 38-Pin ESP32 Boards Differ?

The difference is the development board’s exposed connections and physical layout; it does not mean the 38-pin board has eight more usable GPIOs.

A typical ESP32 pinout 30 pin drawing describes a specific compact DevKit-style board. The official ESP32-DevKitC V4 has two 19-position headers, including supply, ground, control and flash-related contacts. Do not transfer a wire by its position from one format to the other.

The table below is a connector lookup for ESP32-DevKitC V4 with a WROOM module. Numbers are J2/J3 connector positions from Espressif’s header tables, not GPIO numbers. Confirm orientation against the board before wiring.

Position J2 label / signal J3 label / signal
1 3V3 GND
2 EN IO23
3 VP / GPIO36 IO22
4 VN / GPIO39 TX / GPIO1
5 IO34 RX / GPIO3
6 IO35 IO21
7 IO32 GND
8 IO33 IO19
9 IO25 IO18
10 IO26 IO5
11 IO27 IO17
12 IO14 IO16
13 IO12 IO4
14 GND IO0
15 IO13 IO2
16 D2 / GPIO9 — flash IO15
17 D3 / GPIO10 — flash D1 / GPIO8 — flash
18 CMD / GPIO11 — flash D0 / GPIO7 — flash
19 5V CLK / GPIO6 — flash

Which ESP32 Pins Need Special Care?

Flash connections, input-only pins, strapping pins and module-specific PSRAM connections need review before they are connected to external hardware.

ESP32 input-only GPIO, boot strapping and flash connections highlighted at their DevKitC V4 header locations
  • GPIO6–11: leave the WROOM flash bus alone, even when the board exposes those contacts.
  • GPIO34–39: use for inputs only. A floating switch input needs an external bias resistor.
  • GPIO0: holding it low during reset selects serial download mode under the appropriate boot configuration.
  • GPIO12: a high reset-time level can select 1.8 V for VDD_SDIO unless overridden by configuration. That can prevent a board using 3.3 V flash from booting.
  • GPIO16/17: available on the WROOM-based DevKitC reference, but reserved on WROVER variants.

GPIO4 is not one of the classic ESP32’s five strapping pins. It can still be occupied by board hardware, so “not a strap” is not the same as “unused.” Check boot behavior with the peripheral attached and powered, not only with an unloaded board.

Can ESP32 Pins Use 5 V?

Do not apply 5 V to an ESP32 GPIO or the 3V3 rail. A development board’s 5V power input feeds its supply circuitry; it does not change the GPIO logic voltage.

  • Connect 3.3 V peripherals using compatible signal levels and a common ground.
  • Use suitable level translation when a peripheral drives 5 V signals toward the ESP32.
  • Check sensor breakout-board pull-ups: a board powered from 5 V may also pull SDA/SCL up to 5 V.
  • For DevKitC V4, use only one documented supply method at a time: USB, 5V/GND, or regulated 3V3/GND.

For a custom classic ESP32 design, Espressif recommends a 3.3 V supply capable of at least 500 mA. This is supply capability, not a claim that the device always consumes 500 mA. Include peripheral demand and transient performance when selecting the regulator. A weak supply can appear to be a pinout problem when the board resets during radio activity.

Which Pins Should You Use for I2C, SPI and UART?

GPIO21/22 are the Generic ESP32 Arduino I2C defaults; GPIO18/19/23 with GPIO5 are a common VSPI mapping; GPIO1/3 are UART0 TX/RX. Firmware can route many peripheral signals to other eligible pins.

Interface Example mapping Important condition
I2C SDA 21, SCL 22 Pull-ups to the compatible logic rail; defaults vary by board definition
SPI / VSPI SCLK 18, MISO 19, MOSI 23, CS 5 GPIO5 is a strap; use another configured CS if the peripheral creates a reset conflict
UART0 TX 1, RX 3 Sharing with the USB bridge can interfere with upload or logs
Additional UART example TX 17, RX 16 Explicitly configure the mapping; WROOM example, not WROVER
Classic ESP32 signal connection examples for I2C, SPI and UART showing GPIO assignments, signal directions and common ground

For a compatible 3.3 V sensor, connect VCC to 3V3, GND to GND, SDA to GPIO21 and SCL to GPIO22, then configure the same pins in firmware. The diagram shows signal connections, not physical header positions. SDA/SCL pull-ups must be provided on the sensor board or in your circuit.

Choose I2C pull-up resistance from bus capacitance, speed and device limits rather than treating one resistor value as universal. For UART, connect the ESP32 TX to the peripheral RX and the ESP32 RX to the peripheral TX. RS-232 and RS-485 require the appropriate transceiver; neither connects directly to GPIOs.

Which Pins Support ADC, DAC, PWM and Touch?

Classic ESP32 ADC1 inputs support analog sensing without the ADC2/Wi-Fi conflict; GPIO25 and GPIO26 provide DAC outputs; PWM uses eligible output GPIOs; touch sensing uses a defined subset of pins.

  • ADC1: GPIO32–39 at chip level, with GPIO32, 33, 34, 35, 36 and 39 accessible on the DevKitC reference.
  • ADC2: GPIO0, 2, 4, 12–15 and 25–27; analog access conflicts with Wi-Fi on the classic ESP32.
  • DAC: two 8-bit channels on GPIO25 and GPIO26.
  • PWM: choose an output-capable, otherwise available GPIO and configure the LEDC peripheral.
  • Touch: GPIO0, 2, 4, 12–15, 27, 32 and 33 on the classic ESP32.

ADC range depends on attenuation and calibration; a 3.3 V logic supply does not promise accurate 0–3.3 V analog measurement. Check the configured measurement range and the sensor’s maximum output, including transients. The ADC2 restriction concerns analog conversion, not a blanket ban on using every ADC2-capable pin digitally during Wi-Fi operation.

Why Does an ESP32 Stop Booting After Wiring a Peripheral?

First check whether the peripheral changes a strapping level, loads the supply, drives a programming pin or touches the flash bus.

  1. Disconnect the added peripheral and verify the board boots again.
  2. Measure 3V3 and EN during startup. Look for supply dips rather than relying only on a steady-state meter reading.
  3. Check GPIO0 and other straps against the exact module’s boot requirements.
  4. Remove external loading from GPIO1/3 while testing firmware upload.
  5. Verify firmware GPIO names against the schematic; do not use header-position numbers as GPIO numbers.

If the board works until Wi-Fi starts, investigate regulator capacity, wiring resistance and decoupling. If only analog readings fail with Wi-Fi enabled, check whether the sensor is on ADC2. These are different failure mechanisms and need different fixes.

What Changes When You Put an ESP32 Module on a Custom PCB?

A custom board must reproduce the module’s required power, enable, boot and programming connections while respecting its footprint and antenna placement rules.

Conceptual custom ESP32 PCB layout with module antenna beyond the host board edge, power decoupling and programming test access
  • Footprint: match the exact module pad numbering, orientation and exposed ground connection.
  • Antenna: follow the module-specific keepout; do not place copper or components in an area the antenna drawing requires to be clear.
  • Programming: preserve access to the required UART, EN, boot control and ground signals.
  • Test access: provide measurable power rails and useful I/O test points before routing becomes congested.
  • Assembly validation: inspect module joints and verify cold-start, firmware download and the intended peripheral operation.

Our PCB assembly services can support the transition from prototype to assembled hardware. Define the actual test sequence with the build: successful firmware download alone does not prove sensor accuracy, radio performance or behavior with every external load connected.

FAQ About ESP32 Pinout

Is an ESP32 pinout 38 pin diagram valid for every 38-pin board?

No. Matching pin count does not establish matching header order, regulator connections or onboard peripherals. Use the exact board schematic and revision.

Can I use GPIO34 to drive an LED?

No. GPIO34 is input-only on the classic ESP32. Choose an available output-capable GPIO and add suitable current limiting or a driver.

Are VP and VN power connections?

No. On the DevKitC reference, VP maps to GPIO36 and VN to GPIO39. They are input signals, not positive and negative supply terminals.

Does EN mean a normal GPIO?

No. EN controls the chip enable/reset function. Pulling it low resets the chip; it is not a general application output.

Can I reuse a classic ESP32 pin map for ESP32-S3?

No. Use the S3-specific datasheet and development-board schematic. Similar family names do not guarantee compatible GPIO assignments or peripheral features.

Does a USB-C connector mean the ESP32 has native USB?

No. A classic ESP32 development board can use USB-C through a USB-to-UART bridge. The connector shape does not identify how USB communication reaches the chip.

Need Help Moving Your ESP32 Prototype to a Custom PCB?

Bring the exact module part number, schematic and intended pin assignments into the review before PCB layout is finalized. At EBest Circuit, we can discuss fabrication, assembly and the test requirements for your custom board. Contact sales@bestpcbs.com with your design and project requirements.

You may also like

KiCad vs EasyEDA: Which PCB Design Tool Should You Choose?

October 22nd, 2026

KiCad vs EasyEDA comes down to how you want to design and manage your PCB: choose KiCad for an open-source desktop workflow, or EasyEDA for browser access and integrated component sourcing. If offline work matters, consider both KiCad and EasyEDA Pro. The right choice also depends on your team’s experience, project complexity and plans for future revisions.

EBest Circuit (Best Technology) supports the next step with custom PCB fabrication, component sourcing and assembly, from prototypes to production. Turn your KiCad or EasyEDA layout into a build-ready project by sending your manufacturing files and requirements to sales@bestpcbs.com for PCB/PCBA quotation and engineering review.

KiCad vs EasyEDA

KiCad vs EasyEDA: Key Differences at a Glance

KiCad favors local project control and an open-source workflow; EasyEDA favors convenient access to a connected design and ordering environment. Identify the EasyEDA edition before comparing features, because Standard and Pro differ in their tools and file formats.

Comparison Item KiCad EasyEDA
Design environment Desktop application Browser and desktop options
Software model Open source Proprietary, with free access
Project storage Local project files Cloud or local, edition-dependent
Component sourcing Supplier-independent library workflow Integrated LCSC component ecosystem
Manufacturing options Standard fabrication and assembly outputs Integrated ordering and file export

An EasyEDA vs KiCad decision should account for the life of the board: who will maintain it, where its files will be stored and how revisions will reach production.

KiCad vs EasyEDA Pro: How Does Standard Compare?

EasyEDA Pro is the more relevant comparison when you need expanded PCB tools or offline desktop operation. Standard remains useful for straightforward browser-based work, but its capabilities should not be treated as the limits of the whole EasyEDA product family.

  • EasyEDA Standard: A browser-oriented environment for schematic capture and PCB layout, with its own project format and workflow.
  • EasyEDA Pro: A separate environment with desktop offline modes, differential-pair routing, length tuning and internal autorouting.
  • KiCad: An open-source desktop suite with interactive routing, configurable design rules and locally managed project files.

For a KiCad vs EasyEDA Pro evaluation, test the features your board actually needs. If moving an existing Standard project into Pro, keep the original and check the migrated design before continuing development.

KiCad or EasyEDA: Which Is Easier for Beginners?

EasyEDA can reduce the setup needed to start a simple board in a browser. KiCad can be a good first choice when the goal is to learn a desktop workflow that will remain central to future projects. Familiarity, available teaching material and the intended manufacturing route all affect the learning curve.

For a beginner designing a simple PCB, compare KiCad and EasyEDA by completing the same small project in each: draw a schematic, assign footprints, place parts, route connections and inspect the exported board files.

Judge the complete workflow:

  • Part selection: Can you identify the exact component and package without guessing?
  • Error recovery: Can you understand a reported error and correct its cause?
  • Design changes: Can you update a component without losing track of the schematic-to-PCB relationship?
  • Manufacturing output: Can you generate and inspect the files needed to order the board?

A tool that feels quick during schematic entry may still require substantial learning during footprint assignment or production preparation. Neither interface protects a beginner from an incorrect pinout, reversed connector or unsuitable component package.

Are KiCad and EasyEDA Free for Commercial Use?

Yes. Both allow commercial PCB design without purchasing a basic editor license, although their licensing and service models differ.

  • KiCad: Open-source software that can be used for commercial designs without requiring those designs to be published. Its official libraries include a license exception permitting use in commercial and closed designs.
  • EasyEDA: Free use includes commercial projects, with optional paid services. Check the current plan for storage, support and other service limits before adopting it across a team.
  • Third-Party Libraries: Community projects, downloaded circuit designs and external libraries may have separate licenses. The editor’s commercial-use permission does not automatically cover those assets.

Choose based on the permissions and services your project needs, not the word “free” alone.

How Do Offline Access, File Storage and Collaboration Compare?

KiCad works primarily with local project files; EasyEDA offers cloud workflows, while Pro also supports semi-offline and fully offline desktop modes. Collaboration depends on how the team manages access and revisions, not simply where the editor runs.

  • Offline access: Make sure the project and required libraries are available locally. Editing a board offline is different from accessing a live component catalog.
  • Revision control: KiCad supports Git workflows for tracking changes. Teams still need agreed editing responsibilities to avoid conflicting changes to the same design.
  • Shared projects: For EasyEDA, verify access permissions and collaboration functions against the chosen edition, operating mode and service plan.

Keep a recoverable archive of the editable design and its required library data. This allows another engineer to continue the project without depending on the original designer’s computer or account.

How Do Component Libraries and Footprint Checks Compare?

EasyEDA simplifies part selection within its connected component ecosystem, while KiCad supports official, custom and third-party libraries. Neither approach eliminates footprint verification. A convenient library entry still needs to match the exact component you intend to assemble.

Check production components for:

  • Pin mapping: Schematic pin numbers must match the correct footprint pads.
  • Package dimensions: Confirm pad pitch, body size, exposed pads and mounting features against the datasheet.
  • Orientation: Check pin-one marks, diode polarity and connector mating direction.
  • Assembly details: Review mask and paste openings, component clearances and special soldering requirements.
  • Purchasing identity: Record the exact manufacturer part number and approved alternatives in the BOM.

Two regulators can share a package outline but use different pin assignments. Likewise, a distributor code alone may not give a different assembly supplier enough information to source the intended part.

KiCad vs EasyEDA

How Do PCB Routing and Design Rule Checks Compare?

KiCad and EasyEDA Pro both offer routing and design-rule tools for more than basic boards. The useful comparison is how well each handles your layout constraints and makes violations visible.

  • KiCad routing: Interactive shove and walk-around modes, differential-pair routing and length tuning.
  • EasyEDA Pro routing: Differential-pair and length-tuning functions, plus internal autorouting.
  • Rule checking: Evaluate track widths, clearances, via dimensions and copper-to-edge spacing against the intended fabrication process.

Automation can help complete connections, but it does not establish that a route has a suitable return path or avoids sensitive circuitry. Review critical power, analog and high-speed nets regardless of how they were routed.

DRC and manufacturing DFM serve different purposes. DRC checks the rules configured in the editor; DFM review evaluates the released design against the fabrication and assembly processes. A clean DRC report does not prove signal integrity, thermal performance or complete manufacturability.

How Do You Export from EasyEDA to KiCad?

Export a supported EasyEDA project archive, then import it through KiCad’s project manager. KiCad 10 supports EasyEDA Standard backup ZIP files and Pro projects in supported EPRO or ZIP formats.

  1. Archive the original design. Keep the editable source and reference manufacturing outputs.
  2. Export the project. Use a supported project backup or export, not a fabrication-only ZIP.
  3. Import into a separate KiCad project. Choose the appropriate non-KiCad import option in the project manager.
  4. Review the conversion. Check connectivity, symbols, footprints, layers, copper zones, board outline and design rules.
  5. Verify new outputs. Run schematic and PCB checks, refill copper zones where needed, and compare the manufacturing outputs before release.

If you search for ways to export from EasyEDA to KiCad, you may also encounter easyeda2kicad. That Python tool converts component symbols, footprints and 3D models into KiCad library assets; it is not a mandatory step for importing a complete board.

Which Manufacturing Files Can You Export from Each Tool?

KiCad and EasyEDA can both generate PCB fabrication and assembly files. Complete the package with drawings and project-specific specifications where required.

Manufacturing File Main Purpose
Gerber files PCB layers and board outline
NC drill files Drilled holes and slots
BOM Component identities and quantities
Pick-and-place file Component locations, sides and rotations
Fabrication drawing Stackup and fabrication specifications
Assembly drawing Placement and assembly instructions

EasyEDA’s integrated ordering does not require you to use a particular manufacturer; standard outputs can be sent to another supplier for review. EBest Circuit can use your manufacturing package, board requirements and quantity for PCB/PCBA quotation and engineering review.

Before sending the files:

  • Gerber and drill files: Check layer alignment, board outline, holes and slots in a viewer.
  • BOM and placement data: Match reference designators, fitted parts, board sides and rotations to the intended assembly.
  • Revision consistency: Ensure every file and drawing belongs to the same approved revision.
KiCad vs EasyEDA

KiCad vs EasyEDA: Which Is Better for Your Project?

Choose KiCad for an open-source desktop workflow, EasyEDA for browser access and integrated sourcing, and either tool when its outputs meet your manufacturing needs. For an existing design, the benefits of switching should justify the migration and revalidation effort.

Project Requirement Recommended Tool Key Reason
Browser-based PCB design EasyEDA Convenient online design workflow
Open-source desktop design KiCad Direct control over project files
Integrated component sourcing EasyEDA Connected LCSC component ecosystem
Offline PCB design KiCad / EasyEDA Pro Local desktop workflow options
Existing project maintenance Current design tool Avoid unnecessary migration and revalidation
Independent PCB manufacturing Either Standard fabrication and assembly outputs

Both can support professional PCB work. Project complexity alone does not determine the winner: team experience, verified libraries and a repeatable review process matter. Before committing, take one representative board through design, checking and manufacturing-file export.

FAQs About KiCad vs EasyEDA

Can KiCad and EasyEDA simulate circuits?

KiCad includes an ngspice-based simulator, and EasyEDA Pro supports simulation from version 3.2 using Simulide and NGSpice. Both require suitable component models; simulation does not replace testing a physical PCB.

Can I use KiCad or EasyEDA on macOS and Linux?

Yes—KiCad provides macOS and Linux versions, and EasyEDA’s browser editor works on those platforms with a supported browser. Check operating-system and hardware requirements before installing a desktop client.

Can Gerber files be converted back into an editable schematic?

Not into a complete, faithful schematic automatically: Gerber files describe board artwork rather than the original schematic structure. KiCad’s Gerber Viewer has limited PCB conversion capability, but it does not reconstruct the original schematic or component-library relationships.

Can I export a STEP model for enclosure design?

Yes—KiCad and EasyEDA Pro support STEP export for mechanical CAD workflows. Confirm that component models are included and correctly positioned before checking enclosure clearances.

Why are components missing from my PCB’s 3D view or STEP export?

A footprint may have no assigned model, an unavailable model path or a model format unsuitable for the selected export. In KiCad, check the footprint’s model assignment and file path; EasyEDA Pro’s STEP export requires compatible STEP component models.

Ready to manufacture your PCB after comparing KiCad vs EasyEDA? Send your PCB files to EBest Circuit at sales@bestpcbs.com for fabrication and assembly support.

You may also like

What Is a Diplexer? RF Operation, Uses and PCB Design

October 16th, 2026

A diplexer is a passive, three-port RF network that combines or separates signals in two different frequency bands. One common port carries both bands, while two filtered ports route each band to its intended circuit. It allows an antenna or cable to serve two frequency ranges without using a broadband power splitter. The useful distinction is frequency-selective routing: a diplexer sends each band along a different path rather than dividing every signal between two outputs. Its performance depends on the passbands, insertion loss, isolation, impedance matching and the PCB connections around it.

Illustrative three-port diplexer module with common, low-band and high-band connectors

Key Takeaways

  • A diplexer has one common port and two frequency-selective branch ports; it can separate or combine two bands.
  • A diplexer is not a broadband splitter. It does not inherently impose the ideal splitter’s 3 dB power division on each wanted signal.
  • A duplexer separates transmit and receive paths; a diplexer separates frequency bands. The application and port specifications matter more than the name alone.
  • Match the complete operating bands and system impedance. A 75Ω cable-network component is not a drop-in replacement for a 50Ω RF component.
  • Insertion loss, return loss, isolation and power handling describe different requirements and must be checked separately.
  • PCB stackup, ground connections, land patterns and connector launches can change the assembled circuit’s RF response.
  • For a two-port VNA measurement, terminate the unused third port with the specified impedance and repeat measurements for the remaining paths.

What Is a Diplexer Used For?

A diplexer is used to share one RF connection between two frequency bands, such as separate wireless bands, GNSS bands or cable-network upstream and downstream bands.

  • Wireless equipment: connect two band-specific circuits to a common antenna connection, provided the antenna supports both bands.
  • GNSS receivers: separate selected satellite-navigation frequency ranges for their corresponding receiver paths.
  • Cable networks: separate lower-frequency upstream signals from higher-frequency downstream signals.
  • RF test and amplifier systems: combine different-band signals into a shared connection or separate them before measurement.

At EBest Circuit, we support the PCB and assembly work around these RF circuits. Our RF PCB manufacturing service can review the specified laminate, stackup and impedance requirements before fabrication. The diplexer itself remains a selected RF component or a customer-designed filter network.

How Does a Diplexer Work?

A diplexer works by presenting a low-loss path to the intended frequency band and a rejecting path to the other band at a shared junction.

A common arrangement uses a low-pass filter for the lower band and a high-pass filter for the upper band. Other designs use two band-pass filters. The filters must work together at the common port; joining two independently designed filters with a simple T-junction does not automatically produce a well-matched diplexer.

Conceptual diplexer circuit diagram showing a common junction and two filtered branches

The diplexer circuit diagram above shows the routing concept, not a component-level circuit ready for fabrication. Actual implementations may use lumped inductors and capacitors, LTCC structures, distributed transmission lines or other resonant structures.

In a typical reciprocal passive network, signals can travel in either direction. A diplexer combiner therefore uses the two branch ports as inputs and the common port as the combined output. This does not translate frequencies: a 2.4 GHz input remains a 2.4 GHz signal.

What Is the Difference Between a Diplexer, Duplexer and Splitter?

A diplexer separates frequency bands, a duplexer separates transmit and receive paths, and a splitter divides an input signal between outputs. For a closer look at TX/RX isolation and device selection, see our diplexer vs duplexer comparison.

Device Main function Typical arrangement
Diplexer Combine or separate two frequency bands Common port, lower-band port, upper-band port
Duplexer Isolate transmitter and receiver paths Antenna, TX and RX ports; frequency-selective types use different TX/RX bands
Two-way splitter Divide power across two outputs over its operating band One input, two outputs carrying the same input spectrum

An ideal equal two-way splitter sends half the input power to each output, corresponding to about 3 dB per path before excess loss. A diplexer does not make that equal division for an in-band signal; its wanted-path loss comes from the practical filter and interconnect.

The terms diplexer and duplexer sometimes overlap in commercial descriptions. TDK distinguishes multiband separation from TX/RX separation in its RF guidance. For a real design, check the port functions, passbands and required transmitter-to-receiver isolation rather than choosing by product name alone.

Which Diplexer Specifications Matter Most?

The essential specifications are passband limits, insertion loss, return loss, branch isolation, power handling and nominal impedance.

  • Passbands: check both band edges, not only the center frequencies. A filter specified through 5.95 GHz should not be assumed to cover the entire 6 GHz Wi-Fi band.
  • Insertion loss: measures attenuation through the wanted path. As a power calculation, 1 dB loss leaves about 79.4% of the input power at the output under matched conditions.
  • Return loss: describes mismatch at a specified port. A 20 dB return loss corresponds to 1% reflected power at the measurement reference plane.
  • Isolation: describes unwanted coupling between specified ports over specified frequencies. An illustrative 30 dBm input with 40 dB isolation produces −10 dBm leakage, which may still be excessive for a sensitive receiver.
  • Power rating: check average and peak limits, temperature derating and any specified load-mismatch conditions.
  • Impedance: use the component’s specified 50Ω or 75Ω environment, including measurement fixtures and terminations.
Illustrative low-band and high-band transmission curves with a transition region

The transition region between usable bands must fit the system’s frequency plan. The illustration shows the principle only; component acceptance requires the manufacturer’s limits and measured response, not this conceptual curve.

Which Diplexer Filter Fits Your Frequency Bands?

The correct diplexer filter covers both required bands at the system’s nominal impedance and meets the loss, isolation and assembly requirements.

These published Mini-Circuits examples show why frequency range and impedance should be selected before package size:

Model Lower band Upper band Impedance Implementation detail
DPGE-252-492R+ 2400–2500 MHz 4900–5950 MHz 50Ω LTCC, 2.0 × 1.25 mm package
DPLC-8510A0+ DC–85 MHz 102–1220 MHz 75Ω Datasheet states that it is not designed for reflow soldering

The first example serves widely separated GHz bands; the second addresses a cable-network frequency split. They are not interchangeable. Likewise, a frequency range starting at DC does not establish every possible DC-feed connection: verify the pin-to-pin DC path and current rating before using a branch to power an active antenna or other device.

How Does Diplexer Design Affect PCB Layout?

Diplexer design affects PCB layout through the reference impedance, filter junction, grounding and parasitic coupling between the two branches.

For a packaged device, start with the exact manufacturer land pattern and evaluation-board layout. For a discrete filter, include the board stackup and component parasitics in the design model rather than treating the schematic as the complete RF circuit.

Microstrip cross-section identifying signal trace width, dielectric thickness and ground plane
  • Control the transmission-line geometry. Trace width depends on dielectric thickness, dielectric constant, copper thickness and the selected line structure. There is no universal 50Ω trace width.
  • Keep a continuous return path. Avoid reference-plane splits beneath RF traces. Place ground connections and vias according to the component’s recommended layout.
  • Limit coupling between branches. Avoid long parallel runs between the low- and high-band paths. Review spacing and shielding where the isolation budget is tight.
  • Review connector launches. Connector pads, ground transitions and test-access stubs can introduce mismatch that is absent from the component datasheet.
  • Preserve the approved stackup. Changes in dielectric thickness or laminate type can change impedance and filter behavior; review them before fabrication.

Our manufacturing review focuses on whether the specified material, copper features, stackup and assembly footprint can be reproduced. Circuit simulation and RF acceptance limits should remain tied to the actual design and selected components.

How Do You Test a Diplexer?

Test a diplexer with a vector network analyzer by measuring wanted-path insertion loss, port return loss and unwanted branch coupling across the required frequency ranges.

  1. Identify the common, low-band and high-band ports from the device drawing, not their physical position alone.
  2. Calibrate the VNA for the connection arrangement and reference planes. Account for adapters, cables and PCB fixtures.
  3. Connect two measurement ports to the common and low-band paths, and terminate the unused high-band port in the specified impedance.
  4. Repeat for the common-to-high-band path. Then measure branch-to-branch coupling with the common port terminated.
  5. Check return loss at each relevant port and compare the results with limits defined over frequency.
Two-port VNA connected to common and low-band ports with the high-band port terminated

A multiport VNA can reduce reconnections. With either arrangement, measurement power must stay within the component and instrument ratings. Small-signal measurements alone do not establish high-power performance, thermal behavior or receiver protection under an actual transmitter load.

What Causes High Loss or Poor Isolation?

Unexpected loss or poor isolation commonly comes from incorrect port connections, impedance mismatch, layout coupling, assembly defects or an unsuitable measurement fixture.

  • Loss increases near a band edge: check whether the operating frequency is outside the guaranteed passband.
  • Both paths show poor matching: inspect the common-port launch, ground connections and calibration plane.
  • Isolation is worse on the assembled board: investigate coupling around the filter, including parallel traces and shared return paths.
  • Results change when cables move: check connector integrity, cable stability and calibration.
  • Only some boards fail: inspect solder joints, component orientation and substitutions before changing the RF design.

For prototype troubleshooting, compare the board with the manufacturer’s evaluation arrangement where available. This helps separate component behavior from PCB and fixture effects.

FAQ About Diplexers

Can a diplexer separate two signals at the same frequency?

No. Its routing is frequency-selective, so it cannot distinguish two signals occupying the same frequency solely because they come from different sources.

Does a diplexer need a power supply?

A conventional passive diplexer does not need a separate supply. A larger module may include powered switches or amplifiers, which must be checked separately.

Can a diplexer circuit use FR-4?

Yes, when the selected FR-4 system, routing length and frequency meet the circuit’s loss and impedance requirements. Higher-frequency or tighter-loss designs may require a lower-loss laminate; there is no single frequency cutoff for every board.

What is the difference between a diplexer and a triplexer?

A diplexer separates two bands using three ports. A triplexer separates three bands and typically has one common port plus three band-specific ports.

What is the difference between a circulator and a diplexer?

A circulator routes signals between ports in a defined nonreciprocal sequence. A conventional diplexer routes signals according to frequency and is generally reciprocal.

How Can EBest Circuit Support Your RF PCB Project?

We support RF PCB fabrication and PCB assembly for customer-designed circuits, including boards that integrate diplexers and associated RF components.

For these projects, our review can address the specified laminate and stackup, impedance-controlled routing requirements, component footprints and assembly constraints. Identify any components that cannot follow the standard reflow process before production. RF test methods, fixtures and acceptance limits should be agreed as part of the project scope.

Contact sales@bestpcbs.com to discuss your RF board. Share the board files and selected diplexer datasheet so we can review the manufacturing and assembly requirements with your team.

You may also like

Diplexer vs Duplexer: Differences and RF Selection

October 16th, 2026

Diplexer vs duplexer comes down to the job the RF network performs: a diplexer combines or separates two frequency bands at a common port, while a duplexer separates a transmitter and receiver sharing an antenna. A common filter-based duplexer uses different transmit and receive frequencies, not the same frequency. Both devices can be passive, and their circuit structures can overlap. Choose by the operating bands, insertion loss, isolation and power requirements—not by the product name alone. On a PCB, grounding, matching and coupling between traces also determine whether the selected device delivers its specified performance.

Illustrative RF diplexer module and cavity duplexer shown side by side

Key Takeaways

  • Diplexer vs duplexer is primarily a distinction between frequency-band routing and transmit/receive separation, not between passive and active components.
  • A diplexer filter connects two frequency-selective branches to one common port; signals can travel in either direction through a suitable reciprocal network.
  • Most familiar frequency-division duplex (FDD) filter duplexers use separate TX and RX bands. Sharing an antenna does not mean sharing one frequency.
  • A shared-antenna repeater needs enough isolation to prevent transmitter leakage and noise from degrading reception.
  • A splitter divides power over a shared frequency range; a diplexer routes different bands and does not inherently impose a 3 dB power split.
  • Insertion loss, return loss, port-to-port isolation, power handling and operating temperature must be checked against the actual band plan.
  • PCB trace coupling can bypass a filter. Verify the assembled RF path, not just the component datasheet.

What Is the Main Difference Between a Diplexer and a Duplexer?

A diplexer separates signals by frequency band; a duplexer provides the transmit/receive separation needed by a shared-antenna radio. These descriptions identify different functions, so the terms are not always mutually exclusive.

Feature Diplexer Filter-based duplexer
Main function Combine or separate two frequency bands Separate TX and RX paths at one antenna
Typical port labels Common, low band, high band Antenna, TX, RX
Frequency relationship Two distinct passbands Paired TX and RX bands in an FDD system
Selection priority Passband coverage, loss and branch isolation TX/RX isolation, loss and transmitter power
Example use Two radio bands sharing a feedline Cellular front end or shared-antenna repeater
Possible construction LC, distributed, ceramic or other filter networks SAW, BAW, cavity or other suitable filter networks

TDK’s terminology guidance distinguishes band separation from transmission/reception separation. In practice, a frequency-selective network may serve both roles. Check the port diagram and specifications whenever a supplier uses the names differently.

At EBest Circuit, we support the PCB fabrication and assembly work around RF components. Our RF PCB manufacturing support connects the approved laminate, stackup and impedance requirements to the board that carries the filter network.

How Does a Diplexer Filter Route Two Frequency Bands?

A diplexer filter sends each frequency band through its intended branch while rejecting that band at the other branch. The common port carries both bands together. Our diplexer guide explains the filter arrangement, circuit diagram and component specifications in more detail.

For example, Mini-Circuits’ DPGE-252-492R+ is specified for 2.4–2.5 GHz and 4.9–5.95 GHz. Those passbands illustrate band routing: the lower-band radio and higher-band radio connect to different branches, while a suitable shared antenna or feedline connects to the common port.

  • Combining: each branch feeds its band toward the common port.
  • Separating: the common-port signal is filtered into the two branches.
  • Isolation: attenuation between branches limits unwanted interaction between the connected circuits.

The filter does not shift a signal to a different frequency. A 2.4 GHz input stays at 2.4 GHz; it is routed, not converted.

Two frequency bands combine at a diplexer common port through separate filter branches

Does a Duplexer Use the Same Transmit and Receive Frequency?

A conventional FDD filter duplexer uses different transmit and receive bands. It allows both paths to operate simultaneously through a shared antenna while filtering unwanted energy between them.

Qorvo’s TQQ7101 is a documented BAW duplexer example covering 1,920–1,980 MHz and 2,110–2,170 MHz in a 3 × 3 mm package. It is discontinued and is cited here only to show a real frequency plan—not as a recommendation for a new BOM. Uplink and downlink exchange TX/RX roles depending on whether the equipment is a handset or a base station.

Same-frequency simultaneous transmission and reception require a different isolation strategy, potentially including nonreciprocal routing and self-interference cancellation. A pair of ordinary band filters cannot distinguish two signals occupying the same frequency solely by which direction they travel.

Separate 1920 to 1980 MHz and 2110 to 2170 MHz bands in an example FDD frequency plan

Do You Need a Duplexer for a Repeater?

A repeater that transmits and receives simultaneously through one antenna normally needs a duplexer or another engineered isolation arrangement. Separate antennas can provide part of the isolation, but their separation alone does not guarantee acceptable receiver performance.

The receiver must detect a weak wanted signal while a nearby transmitter produces much greater RF power. Two checks matter:

  • TX carrier rejection: keep the strong transmit signal from overloading the receiver front end.
  • TX noise rejection in the receive band: keep transmitter noise from raising the receiver’s effective noise floor.

A broad VHF/UHF diplexer is therefore not an automatic substitute for a duplexer serving a closely spaced pair of repeater channels. Its passbands may route both repeater frequencies through the same branch.

How Much Isolation Does the RF System Need?

Required isolation comes from transmitter power and the receiver’s allowed interference level at the frequency being evaluated; there is no single correct isolation value for every diplexer or duplexer.

For a simple carrier-leakage estimate:

Required isolation (dB) = TX power (dBm) − allowed leakage at RX (dBm).

If a hypothetical transmitter produces +30 dBm and the chosen receiver limit at that interferer frequency is −30 dBm, the path needs at least 60 dB isolation before adding design margin. With only 40 dB isolation, the estimated leakage would be −10 dBm. These are calculation inputs, not universal receiver limits or EBest Circuit test results.

This estimate does not replace a receiver blocking or desensitization test. Transmitter noise inside the RX band, antenna mismatch and coupling around the filter require separate evaluation.

Illustrative isolation calculation showing plus 30 dBm transmitter power minus 60 dB isolation equals minus 30 dBm leakage

Which Specifications Should You Compare Before Selecting a Device?

Compare the complete passbands, loss, isolation, power rating and impedance first, then check the package and assembly requirements. Matching the advertised center frequency alone is insufficient.

Parameter Selection basis
Passband, MHz or GHz Both occupied bands, including band edges and tolerances
Insertion loss, dB TX output budget and RX sensitivity budget across each band
Isolation / rejection, dB Specified port pair and frequency; check TX and RX bands separately
Return loss / VSWR Matching at every relevant port under specified terminations
Power, W or dBm Average and peak power, duty cycle, temperature and mismatch conditions
Reference impedance, Ω 50 Ω or 75 Ω system compatibility as applicable
Package and mounting Land pattern, grounding, reflow compatibility and mechanical envelope

For scale, 1 dB of insertion loss passes about 79% of the incident power; 3 dB passes about 50%. Those ratios follow 10−loss/10. On a receiver, loss ahead of the first amplifier also consumes sensitivity margin.

If the system alternates TX and RX in time, evaluate its TDD switch and filtering architecture rather than assuming an FDD duplexer is needed. If several different bands must coexist, a diplexer or higher-order multiplexer may belong ahead of individual band-specific front ends.

What PCB Layout Issues Can Reduce Isolation?

Direct coupling between TX and RX traces, weak ground connections and mismatched launches can reduce assembled isolation even when the filter itself meets its datasheet.

  • Separate the paths: avoid long parallel TX and RX runs that create a bypass route around the component.
  • Maintain the reference plane: do not route RF traces across ground splits; keep return paths continuous.
  • Follow the land pattern: reproduce the specified signal pads, ground pads and local grounding arrangement.
  • Control transmission lines: calculate width and spacing from the actual stackup, dielectric properties and copper geometry.
  • Review shielding: ground a shield enclosure properly rather than treating a metal lid as an automatic isolation improvement.
  • Check assembly: inspect port orientation, bridges and ground-pad solder connections before troubleshooting the RF response.

There is no universal “50 Ω trace width” suitable for every board. A width copied from a reference layout can be wrong when the dielectric thickness or material changes. During our manufacturing review, the approved stackup and fabrication data need to describe the same controlled-impedance structure.

How Should You Test the Assembled RF Paths?

Use calibrated RF measurements to verify insertion loss, return loss and isolation on the assembled network, then check receiver performance with the transmitter operating under the intended conditions.

  1. Calibrate the vector network analyzer to the chosen reference planes and account for fixture or cable loss.
  2. Measure common-to-branch transmission across each passband.
  3. Measure branch-to-branch isolation across the required interference bands.
  4. Terminate unused ports in the specified impedance; an open port can change the network response.
  5. Verify powered-system behavior separately, including receiver desensitization and permitted TX power conditions.

For a three-port device, label the ports before interpreting S-parameters: S21 only means transmission from port 1 to port 2, not automatically “TX-to-antenna loss.” Also check instrument dynamic range; an apparent isolation floor may belong to the fixture or instrument.

Three-port RF network measurement with two analyzer connections and the unused branch terminated

For PCB assembly, define the inspection scope and any required RF acceptance procedure before production. Electrical continuity and visual solder inspection do not establish an RF isolation result.

FAQ About Diplexer vs Duplexer

What is the duplexer meaning in an RF circuit?

A duplexer connects a transmitter and receiver to a shared antenna while providing separation between their paths. The implementation depends on the radio architecture; a common FDD version uses two frequency-selective filters.

Diplexer vs splitter: can they do the same job?

Not usually. A splitter distributes signals over a common frequency range, while a diplexer routes different bands to different ports. An ideal equal two-way splitter divides power by 3 dB per output before excess loss; a diplexer does not inherently make that equal power division.

Duplexer vs circulator: what is different?

A filter duplexer separates TX and RX using frequency selectivity. A circulator is nonreciprocal and routes energy sequentially between ports. Antenna reflections and finite isolation still matter, so a circulator alone does not guarantee adequate receiver protection or same-frequency full-duplex performance.

Are diplexers and duplexers active components?

Many are passive networks and need no DC supply. An integrated RF module may also contain powered amplifiers or control circuits. Check the module schematic rather than classifying the whole assembly from the filter name.

Can you tune every diplexer or duplexer?

No. Some cavity assemblies have adjustable resonators, while many surface-mount ceramic, SAW and BAW devices have fixed responses. Tune only devices intended for adjustment, using the manufacturer’s procedure and suitable RF instruments.

Can two parts with the same package be interchanged?

No. The port assignment, frequency plan, matching, power rating and soldering requirements must also agree. A matching body size is not evidence of electrical or footprint compatibility.

How Can EBest Circuit Support Your RF PCB Assembly?

We support the board fabrication and assembly needed to turn an approved RF design into hardware. For diplexer or duplexer circuits, discuss the laminate and stackup, controlled-impedance requirements, component land patterns and assembly inspection scope with our team.

Send your RF PCB or PCBA project to sales@bestpcbs.com. Include the component part numbers and any RF acceptance criteria so we can review the manufacturing requirements alongside the board design.

You may also like