PCB manufacturing PCB manufacturing
Home > Blog

Medical Monitoring PCB Assembly Manufacturer | ISO 13485 Certified & Traceability

November 4th, 2026

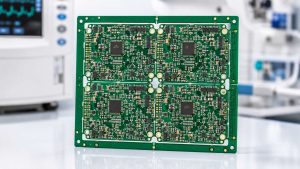
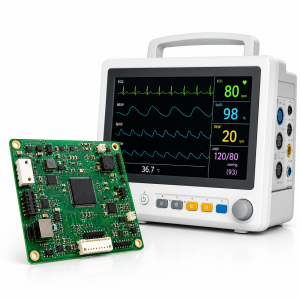
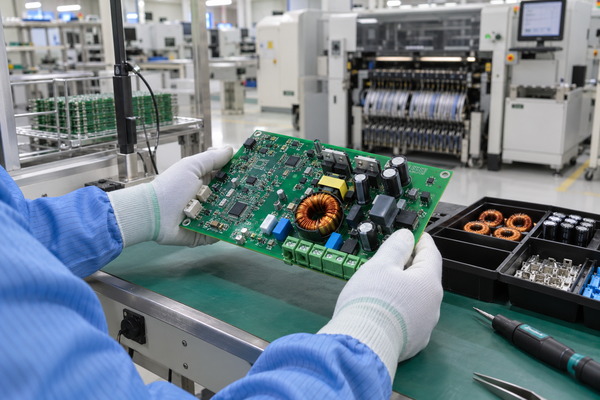
Medical monitoring PCB assembly requires precise soldering, controlled components, and reliable electrical performance. EBest Circuit provides medical monitoring PCB assembly services for ECG monitors, SpO2 devices, patient monitors, and wearable medical electronics, supported by ISO 13485:2016 quality management and MES production traceability.

Need to identify a defective component lot or maintain consistent quality from prototype to mass production? EBest Circuit combines precision SMT/THT assembly, free DFM support, and functional testing services to help medical device manufacturers address these challenges.
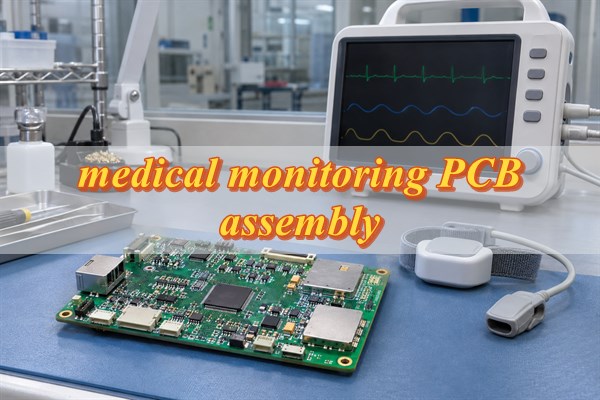
medical monitoring PCB assembly, https://www.bestpcbs.com/blog/2026/11/medical-monitoring-pcb-assembly/

What Types of Medical Monitoring PCB Assemblies Can We Manufacture?

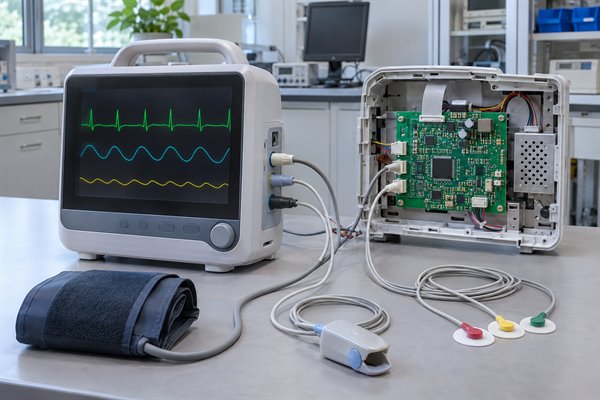
EBest Circuit provides custom PCB manufacturing and assembly for ECG monitors, blood pressure monitors, SpO2 devices, and wearable medical monitoring equipment. Each application requires different approaches to component placement, signal integrity, and assembly verification.
medical monitoring PCB assembly, https://www.bestpcbs.com/blog/2026/11/medical-monitoring-pcb-assembly/
  • ECG monitoring PCB assembly: Analog front-end, filtering, processing, and communication circuits where component accuracy, cleanliness, and reliable electrical connections are important for low-level signal acquisition.
  • SpO2 monitoring PCBA: LED-driver, photodiode-interface, and signal-processing boards requiring correct component polarity, controlled soldering, and interface verification.
  • Multi-parameter patient monitor PCBA: Main control boards, display interfaces, power modules, and sensor-input boards supporting ECG, SpO2, temperature, and non-invasive blood pressure (NIBP) functions.
  • Blood pressure monitor PCB assembly: Pressure-sensor interfaces, pump or valve control circuits, power-management circuits, and connector assemblies.
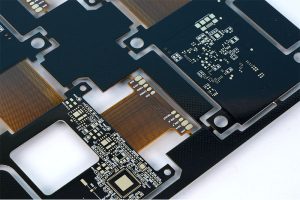
  • Wearable medical monitoring PCBA: Compact rigid, flexible, and rigid-flex circuits requiring fine-pitch assembly, controlled board handling, and accurate component positioning.

Why Choose EBest Circuit for Medical Monitoring PCB Assembly?

EBest Circuit combines precision PCB assembly, medical-device quality management, and engineering support to help medical electronics manufacturers reduce assembly risks and maintain consistent production quality. From initial prototypes to repeat orders, we provide the following services and advantages:

  • Free DFM and engineering support: We review PCB footprints, solder-pad designs, component spacing, polarity, and test-point accessibility before production, helping identify problems that could cause rework or assembly defects.
  • ISO 13485:2016 quality management: Controlled manufacturing documents, inspection procedures, and engineering changes help maintain consistent production requirements across medical monitoring PCBA orders.
  • MES production traceability: Five-year manufacturing history retention supports investigation of material batches, manufacturing abnormalities, and quality concerns using recorded production data.
  • Precision SMT and THT assembly: Support for 01005 components, 0.25 mm BGA pitch, and mixed-technology assembly accommodates compact and densely populated medical monitoring PCBs.
  • One-stop PCB and PCBA manufacturing: We handle PCB fabrication, BOM-based component procurement for PCBA orders, SMT/THT assembly, inspection, and agreed functional testing, reducing the need to manage several manufacturing suppliers.
  • Quality inspection and testing: SPI, AOI, X-ray inspection, and customer-defined functional testing help identify soldering defects, placement errors, and electrical faults.
  • Prototype and mass production support: Initial samples, pilot builds, and repeat orders can be manufactured using controlled BOM revisions, work instructions, and inspection requirements.

What Medical Monitoring PCB Assembly Services Can EBest Circuit Provide?

EBest Circuit offers PCB fabrication, precision assembly, and testing services for medical monitoring electronics. Whether your project requires a prototype or recurring production orders, the assembly scope can be matched to your PCB construction, component specifications, and quality requirements.

  • Prototype PCB assembly: Small-volume assembly for engineering validation, component-fit checks, and initial functional evaluation.
  • Full-turnkey PCB assembly: PCB fabrication, procurement against the approved BOM, SMT/THT assembly, inspection, and packaging within one PCBA manufacturing project.
  • SMT and BGA assembly: Automated placement and reflow soldering for fine-pitch ICs, QFN, QFP, BGA, and miniature passive components.
  • Through-hole and mixed PCB assembly: Installation and soldering of connectors, headers, and other through-hole components alongside surface-mount devices.
  • Flexible and rigid-flex PCB assembly: Assembly services for wearable and portable medical monitoring devices requiring specialized PCB support and handling.
  • PCB inspection and functional testing: Solder-joint inspection, electrical checks, firmware programming, and testing according to customer-approved procedures.
  • Optional box assembly: Integration of assembled PCBs with specified enclosures, connectors, cables, and other mechanical components when required.

For densely populated medical monitoring PCB assemblies, component dimensions and package pitch are important factors in determining assembly feasibility.

Assembly Parameter EBest Circuit Capability
Minimum SMD component 01005
Minimum BGA pitch 0.25 mm
Assembly technologies SMT, THT, mixed assembly
Component packages BGA, QFN, QFP, SMD, through-hole
Component presentation Reel, cut tape, tube, tray, loose parts
PCB constructions supported Rigid, flexible, rigid-flex, multilayer
Assembly lead time 1–5 days for suitable orders

These capabilities are subject to the actual PCB layout, component specifications, assembly requirements, and engineering review.

How Does ISO 13485 Certification Support Medical Monitoring PCB Assembly Quality?

ISO 13485:2016 provides a quality management framework for controlling manufacturing processes, documentation, and production changes in medical electronics manufacturing. For medical monitoring PCB assembly, these controls help reduce inconsistent production practices and support supplier qualification.

  • Manufacturing document control: Approved PCB files, BOMs, placement programs, and assembly instructions help prevent production errors caused by outdated design revisions.
  • Incoming material inspection: PCB and component identities, quantities, packaging conditions, and required batch information are verified against approved manufacturing requirements.
  • Assembly process control: Documented soldering, inspection, and production procedures help maintain consistent manufacturing conditions between orders.
  • Engineering change management: Component substitutions, PCB revisions, and process changes follow the required approval procedures before implementation.
  • Nonconforming product control: Defective or suspect PCB assemblies are identified, evaluated, and handled according to established quality procedures.
  • Corrective and preventive actions: Recorded quality issues support root-cause investigation, corrective actions, and verification of their effectiveness.
  • Quality documentation: Inspection reports, manufacturing records, and relevant quality evidence can support customer audits and investigations within the agreed project scope.

ISO 13485 certification applies to the quality management system within its certified scope rather than individual PCB assemblies. Finished medical-device certification and regulatory approval remain separate from PCBA manufacturing.

How Does EBest Circuit Ensure Medical Monitoring PCB Assembly Traceability?

EBest Circuit uses MES-based production tracking with five-year manufacturing history retention to support medical monitoring PCB assembly traceability. By linking relevant manufacturing records with production batches or individual PCB assemblies, customers can investigate quality problems and identify potentially affected products more efficiently.

  • Component and PCB traceability: Record approved component identities, material lots, date codes, and PCB batch information according to project requirements.
  • BOM and revision control: Associate production orders with approved PCB designs, BOM revisions, assembly drawings, and applicable firmware versions.
  • Manufacturing process records: Track work orders and specified SMT, THT, and inspection activities associated with production batches.
  • Inspection and testing records: Retain agreed inspection results, functional-test outcomes, nonconformance information, and rework verification records.
  • Shipment traceability: Associate finished PCB assembly identifiers or production lots with shipment documentation for future reference.

For example, if an ECG analog-front-end IC is found to belong to a defective supplier lot, recorded material-to-assembly relationships can help identify which PCB assembly batches contain the affected components. The exact traceability fields, individual board identification requirements, and report formats should be established before manufacturing.

How Is Medical Monitoring PCB Assembly Manufactured?

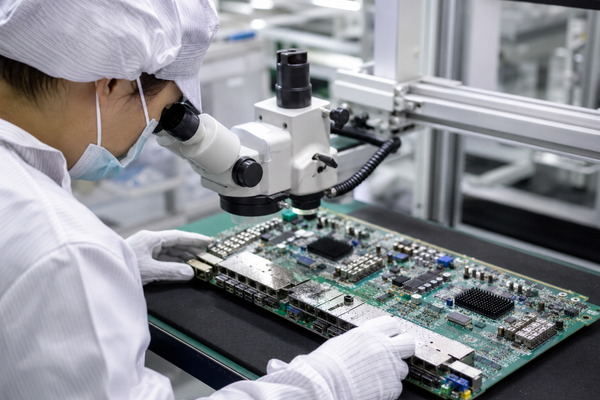
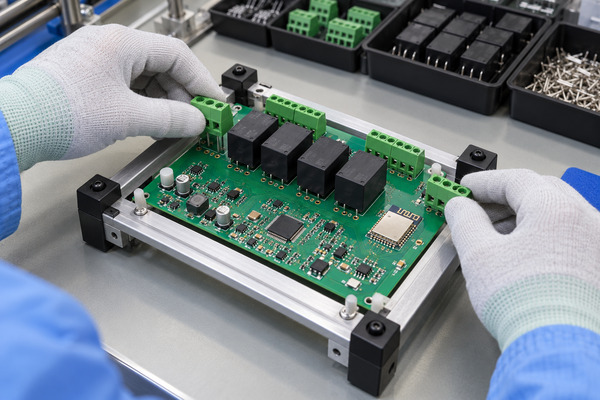
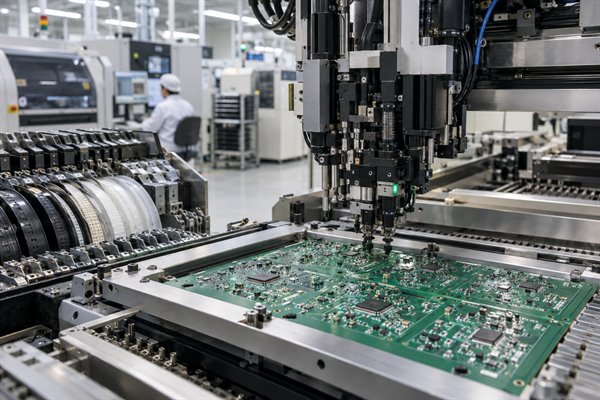
Medical monitoring PCB assembly follows a defined manufacturing process covering PCB fabrication, incoming inspection, precision SMT/THT assembly, and functional verification. EBest Circuit manufactures PCB assemblies according to approved design files and customer-specified acceptance requirements.
medical monitoring PCB assembly, https://www.bestpcbs.com/blog/2026/11/medical-monitoring-pcb-assembly/
  1. Engineering and DFM Review: Check Gerber or ODB++ files, PCB stackup, BOM, component footprints, placement coordinates, solder-pad geometry, polarity, and test-point accessibility. Resolve manufacturing questions before production.
  2. PCB Fabrication: Manufacture the specified rigid, flexible, or rigid-flex PCB. Applicable processes include material preparation, circuit imaging, etching, lamination, drilling, plating, solder-mask application, and surface finishing. Complete bare-board electrical and dimensional inspections.
  3. Incoming Material Inspection: Inspect bare PCBs and verify component part numbers, package types, quantities, polarity markings, and required batch information against the approved BOM.
  4. Stencil Preparation and Solder Paste Printing: Prepare the SMT stencil, secure the PCB panel, and print solder paste onto the pads. SPI is used to inspect solder-paste deposition where required.
  5. SMT Component Placement: Place resistors, capacitors, analog-front-end ICs, microcontrollers, BGA/QFN devices, and other surface-mount components according to the approved placement program.
  6. Reflow Soldering: Solder SMT components using a controlled reflow temperature profile compatible with the solder alloy, component specifications, and PCB materials.
  7. Post-Reflow Inspection: Conduct AOI to identify visible placement and soldering defects. Apply X-ray inspection to hidden BGA/QFN solder joints where required.
  8. Through-Hole Assembly: Install connectors, headers, and other through-hole components using the appropriate manual, selective, or wave-soldering process.
  9. Cleaning and Protective Processing: Perform the specified cleaning process and apply conformal coating when required, with masking for connectors, contact points, and sensitive areas.
  10. Firmware Programming and Functional Testing: Program approved firmware when requested. Verify specified power rails, communication interfaces, sensor-input circuits, and other functions according to the customer’s test procedure.
  11. Final Inspection and Packaging: Confirm assembly acceptance, identification labels, required quality records, and ESD-safe packaging before shipment.

How Are Medical Monitoring PCB Assemblies Inspected and Functionally Tested?

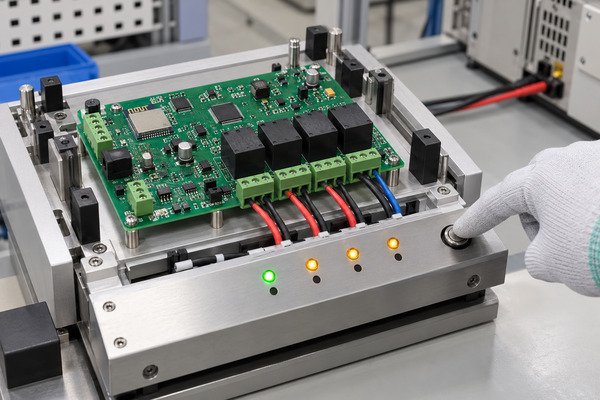
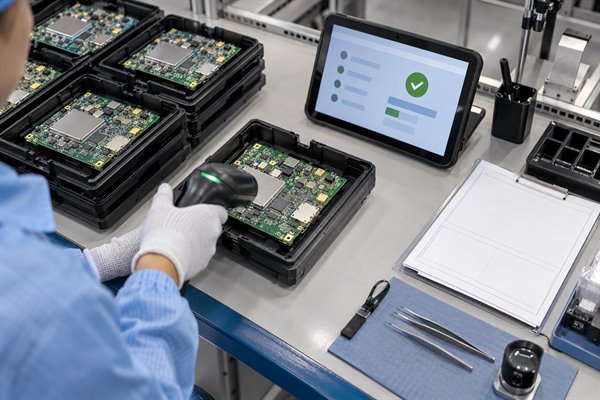
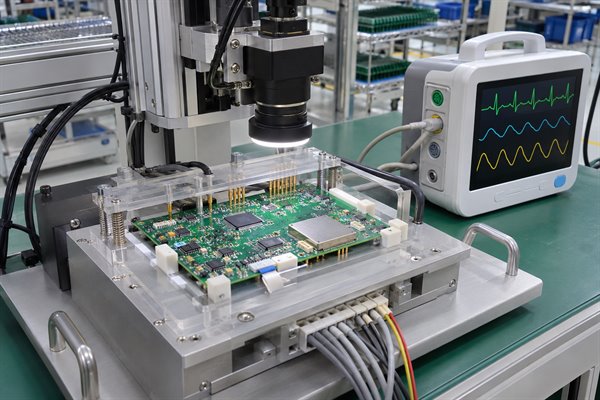
Medical monitoring PCB assemblies require both solder-joint inspection and electrical verification. EBest Circuit uses appropriate inspection methods to identify manufacturing defects and supports customer-defined functional tests to verify the required behavior of ECG, SpO2, and patient-monitoring circuits.
medical monitoring PCB assembly, https://www.bestpcbs.com/blog/2026/11/medical-monitoring-pcb-assembly/
Inspection or Test Inspection Focus Purpose
SPI Solder-paste deposition Detect insufficient, excessive, or misaligned solder paste
AOI Component placement, polarity, visible solder joints Identify missing components, placement defects, and visible soldering problems
X-ray Hidden BGA/QFN solder joints Examine concealed solder connections and selected internal solder defects
ICT / Electrical Checks Accessible circuits and electrical connections Identify shorts, opens, and specified electrical faults
Functional Testing (FCT) Power, signal acquisition, communication, and control functions Verify board functions against customer-approved test limits

For ECG PCB assemblies, functional testing may use a known electrical reference signal to verify acquisition-channel response. SpO2 PCB assemblies may require LED-drive, photodiode-interface, and communication checks. Multi-parameter patient-monitor boards may also require power and display-interface verification.

Test fixtures, input signals, measurement limits, and acceptance criteria are established according to the customer’s specifications. Board-level testing does not replace finished medical-device certification.

What Are the Main Challenges in Medical Monitoring PCB Assembly and How Do We Solve Them?

Medical monitoring PCB assemblies often combine sensitive analog circuits, miniature components, and complex digital interfaces. EBest Circuit addresses the associated manufacturing risks through DFM review, controlled soldering, component verification, and application-specific testing.

  • Low-level ECG signal errors: Incorrect passive component values, solder residues, and poor electrical connections can affect signal acquisition. We verify critical BOM positions, follow specified soldering and cleaning procedures, and support reference-signal testing to identify assembly-related problems.
  • SpO2 sensor-interface faults: Incorrect LED or photodiode polarity and component mismatches may interrupt the signal path. Component verification, polarity inspection, and customer-defined interface tests help identify these defects before shipment.
  • Fine-pitch soldering defects: Dense QFN and BGA packages can develop hidden solder bridges or insufficient solder connections. Stencil design review, controlled placement and reflow, and X-ray inspection where required help detect these problems.
  • Mixed-signal interference: Sensitive analog channels may be affected by switching power supplies or digital circuitry. DFM review identifies layout and assembly concerns, while electrical and EMC tests determine whether the final design meets its performance requirements.
  • Inconsistent production batches: Unapproved component substitutions, obsolete BOM revisions, and manufacturing changes can affect repeat production. Controlled documentation, material verification, and engineering change approval help maintain the approved PCBA configuration.

Medical Monitoring PCB Assembly Case Study: Patient Monitoring Device

EBest Circuit provided medical monitoring PCB assembly services for a patient monitoring device integrating sensor inputs, power management, display connections, and wireless communication. The project required fine-pitch component assembly, functional testing, and traceable manufacturing records.

Project Background

The customer required a medical PCBA integrating sensor input circuits, a microcontroller, power management, display connectors, and a wireless communication module. The assembled boards needed to pass functional verification before the project could proceed to pilot production.

Manufacturing Challenges

The PCB combined sensitive sensor interfaces with densely populated digital and power circuitry. Fine-pitch BGA and QFN packages presented soldering and inspection challenges, particularly because their hidden joints could not be fully examined through visual inspection.

Our Solution

EBest Circuit reviewed the Gerber files, BOM, component polarity, pad dimensions, stencil openings, and test-point accessibility before production.

During SMT assembly, SPI was used to inspect solder-paste deposition, while AOI checked component placement and visible solder defects. X-ray inspection was applied to hidden BGA and QFN solder joints. Functional testing covered power rails, sensor inputs, display connections, and communication interfaces.

Project Results

The prototype passed visual inspection, X-ray inspection, and functional testing. The customer received traceable manufacturing records, and the verified samples supported the transition to pilot production.

What Affects Medical Monitoring PCB Assembly Lead Time?

Medical monitoring PCB assembly lead time depends on PCB fabrication requirements, component availability, assembly complexity, and testing scope. EBest Circuit supports 1–5 days for suitable PCB assembly orders, while complete project delivery schedules depend on the manufacturing and verification requirements.

  • PCB fabrication complexity: Multilayer structures, HDI designs, flexible materials, and special PCB processes may require additional manufacturing time.
  • Component availability: Long-lead analog-front-end ICs, microcontrollers, and specialized medical electronics components can affect material readiness.
  • Assembly requirements: Fine-pitch BGA/QFN packages, double-sided assembly, and mixed SMT/THT processes influence production scheduling.
  • Inspection and testing: X-ray inspection, firmware programming, custom functional-test fixtures, and additional verification may extend the schedule.
  • Order quantity and approval: Prototype, pilot, and mass production orders require different levels of manufacturing preparation and customer approval.

A confirmed lead time should account separately for PCB fabrication, component readiness, PCBA assembly, functional testing, and transportation to the specified delivery location.

FAQs About Medical Monitoring PCB Assembly

Medical monitoring PCB assembly projects may involve different component configurations, material-handling requirements, and packaging specifications. The following answers address common manufacturing questions.

Q1: Can you assemble customer-supplied bare PCBs?

A1: Yes. Customer-supplied PCBs can be assembled after reviewing their condition, surface finish, panelization, and assembly requirements.

Q2: Can selected component positions be left unpopulated?

A2: Yes. Do-not-populate positions should be clearly identified in the approved BOM and assembly drawings.

Q3: Can you manufacture different BOM variants separately?

A3: Yes. Each variant requires its own approved BOM, placement information, and identification to prevent component mixing.

Q4: How are moisture-sensitive components handled before reflow?

A4: Moisture-sensitive components are handled according to applicable storage, floor-life, and baking requirements.

Q5: Can we provide our own PCB panel design?

A5: Yes. Customer-defined panels can be reviewed for fiducials, tooling margins, support requirements, and depanelization clearance.

Q6: Can we specify solder alloy and cleaning restrictions?

A6: Yes. The required soldering materials and cleaning restrictions should be included in the assembly specification for process compatibility review.

Q7: Can connectors and sensitive contacts be masked during conformal coating?

A7: Yes, when conformal coating is included in the project scope. Masking areas should be clearly identified in the coating drawing.

Q8: Can boards receive individual labels and ESD-safe packaging?

A8: Yes. Individual identification labels and ESD-safe packaging can be arranged according to the approved shipment instructions.

How Can You Request a Medical Monitoring PCB Assembly Quote?

EBest Circuit provides custom medical monitoring PCB assembly services, covering PCB fabrication, precision SMT/THT assembly, quality inspection, and functional testing support. Send your Gerber or ODB++ files, BOM, placement data, assembly drawings, quantity, required component date codes, delivery location, and target delivery date to sales@bestpcbs.com. Include your quality, traceability, and testing requirements to receive a project-specific quotation and free DFM review.

Medical monitoring PCB assembly requires more than reliable solder joints. ISO 13485 quality management, MES production traceability, precision assembly, and defined functional testing help medical device manufacturers control production risks and maintain consistent PCB assembly quality. With EBest Circuit’s one-stop PCB and PCBA manufacturing services, customers can move from prototype validation to repeat production with coordinated engineering, manufacturing, and quality support.
You may also like

Aluminum Substrate PCB for Lighting Supplier | Custom LED PCBs

October 29th, 2026

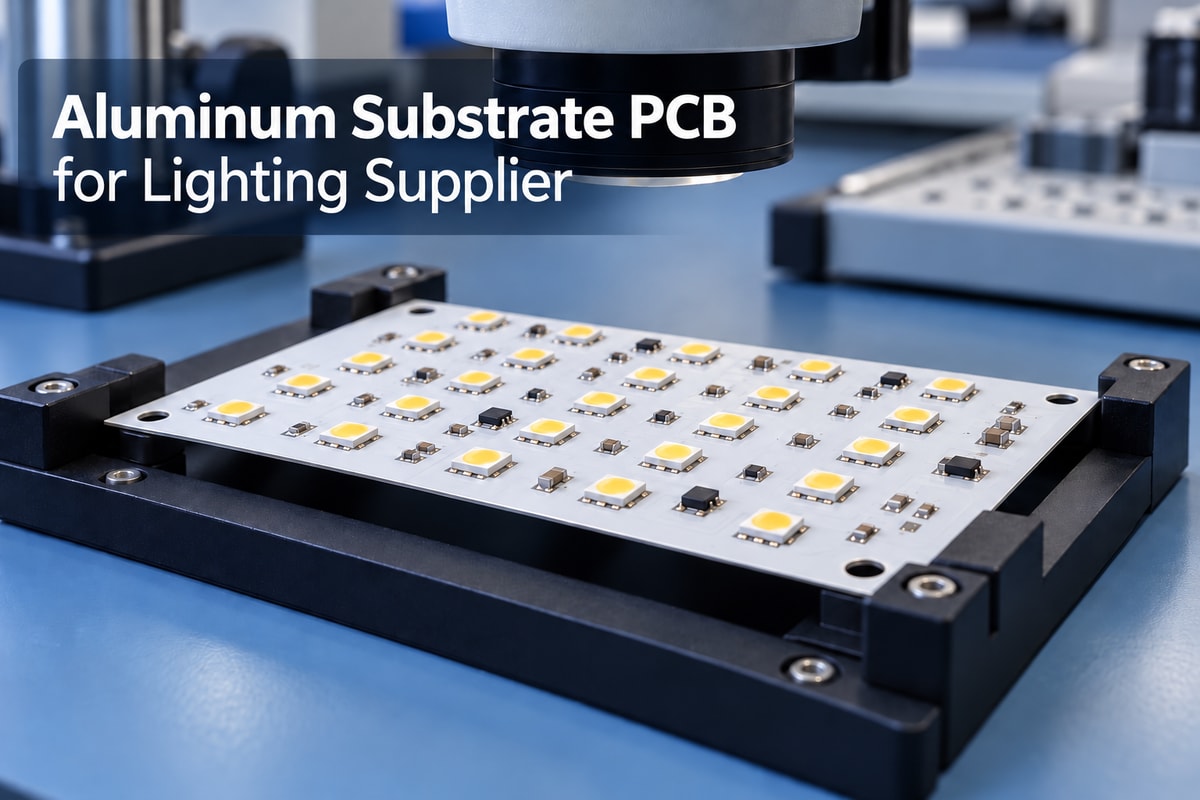
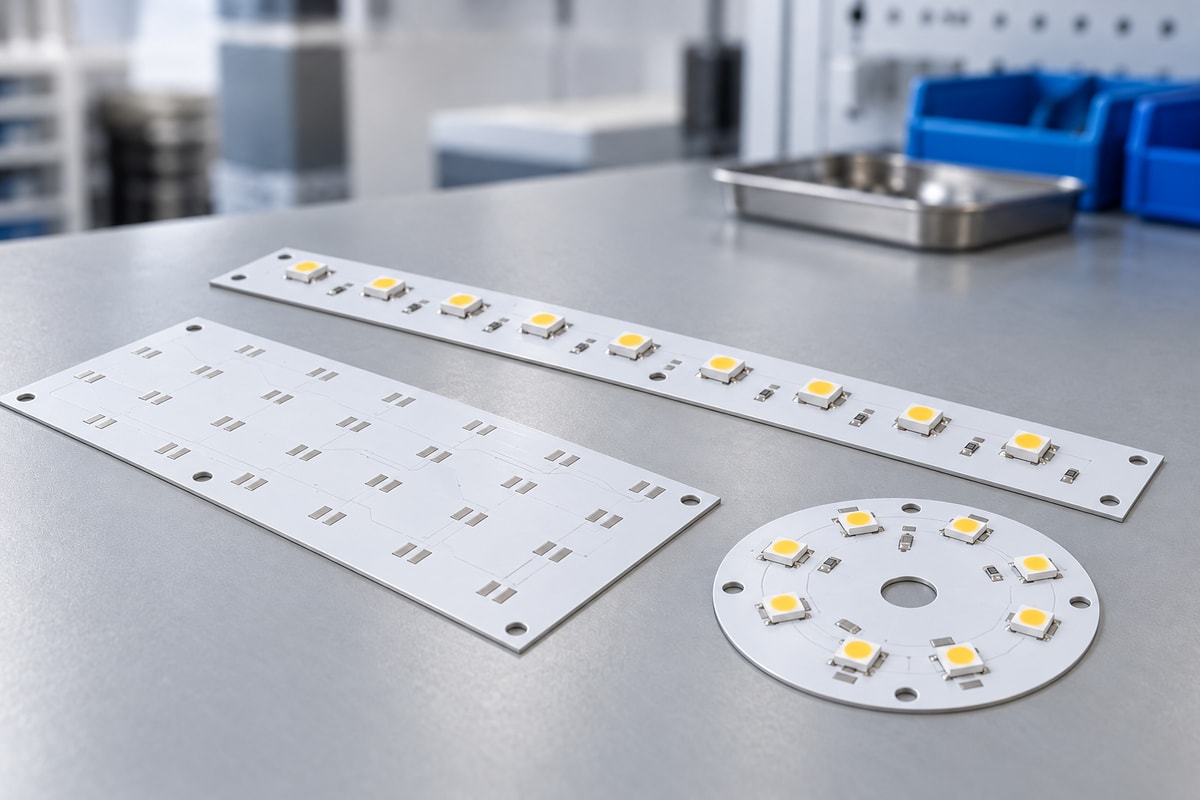
An aluminum substrate PCB for lighting supplier should help you turn an LED design into boards that fit your fixture, support its thermal requirements, and arrive ready for the next production step. For lighting manufacturers, that means dependable PCB fabrication, suitable materials, accurate mounting features, and assembly support when a bare board alone is not enough.

At EBest Circuit (Best Technology), we combine MCPCB manufacturing experience dating back to 2006 with component sourcing and PCB assembly. We support custom lighting boards from prototypes through production, bringing the board and assembly requirements into one coordinated order. Send your drawings and quantity to sales@bestpcbs.com to discuss a bare-board or assembled LED module quotation.

Aluminum substrate PCB for lighting supplier

Top 10 Aluminum Substrate PCB for Lighting Suppliers in China

China offers both online PCB ordering services and manufacturers supporting custom metal-core boards and assembly. The ten suppliers below provide relevant aluminum PCB services. This is a sourcing shortlist based on product and service fit; the order does not represent an independent performance ranking.

Supplier Relevant Products and Services
EBest Circuit (Best Technology) Custom MCPCBs, component sourcing, and LED assembly
PCBWay Online aluminum PCB quotes; material/finish options
JLCPCB Single-layer MCPCBs in defined configurations
ALLPCB Aluminum PCBs within specified machining limits
PCBasic Aluminum PCB fabrication and PCBA services
Viasion Single-sided, double-sided, and multilayer MCPCBs
RayMing / RAYPCB LED arrays and linear-lighting PCB assembly
Hitech Circuits Two-layer and COB aluminum PCB constructions
Venture Electronics Aluminum PCB fabrication and stackup support
WellPCB Aluminum PCB design review and assembly

A standard single-layer LED board and a custom assembled lighting module require different levels of support. At EBest, our emphasis is on coordinating the PCB construction, mounting features, component procurement, and assembly around the customer's lighting design.

Who We Supply: Aluminum PCB for LED Lighting OEMs

Our aluminum PCB service is suited to businesses that build lighting products, LED modules, or assemblies for other brands. The supply scope can match the stage your team wants to handle internally.

  • Lighting OEMs and ODMs: Boards shaped for their housings, optics, and heat sinks, with a manufacturing route that can continue into repeat production.
  • LED Module Manufacturers: Consistent circuit layouts, mounting features, and component placement across a module family.
  • Industrial and Outdoor Lighting Brands: Boards matched to the thermal and mechanical requirements of high-bay lights, street lights, floodlights, and related fixtures.
  • Specialist Lighting Developers: Support for compact optical layouts and application-specific assembly details, including medical-lighting modules.
  • Contract Manufacturers and Lighting Solution Companies: We supply bare aluminum PCBs for their own SMT lines or assembled boards to simplify integration.

For a team with established LED assembly capacity, we can supply the fabricated boards. For a team managing product development and final fixture assembly, we can combine PCB fabrication, component sourcing, and SMT work.

Custom Aluminum PCB Manufacturing Capabilities for Lighting Projects

We manufacture custom aluminum PCBs around the electrical layout and mechanical drawing. Board thickness, copper weight, dielectric selection, and outline processing are reviewed together so that a change intended to improve one feature does not create a problem elsewhere.

Manufacturing Item Specification
Construction Single-sided; double-sided; single-sided two-layer
Board thickness 0.8–3.0 mm routine
Outer-layer copper 1–3 oz; ≥3 oz requires confirmation
Dielectric thermal conductivity 1, 2, 3 W/m·K
Dielectric thickness 100–110 µm; specified Boyu/Juding constructions
Outer-layer line width / spacing, 1 oz 0.20/0.20 mm minimum
Outer-layer line width / spacing, 2 oz 0.25/0.25 mm minimum
Non-plated finished hole Ø1.0 mm minimum; diameter tolerance ±0.05 mm
Outline tolerance ±0.15 mm routine; ±0.10 mm upon review
Solder mask White, black, green; other colors upon review
Surface finish HASL, OSP, immersion gold

Higher dielectric conductivity requires a material enquiry. Other material systems need their own dielectric-thickness specification. Line width and spacing are drawing minima; hole-position tolerances are specified separately from hole-diameter tolerances. Routing and insulation follow the selected stackup, and the surface finish follows assembly requirements.

These options are reviewed as a complete construction; they are not a promise that every process limit can be combined on one board.

Copper weight directly affects routing space. Moving from 1 oz to 2 oz changes the routine line and spacing requirement above. Reviewing this before fabrication helps preserve the intended LED layout without relying on an unsuitable manufacturing assumption.

High Power LED Aluminum PCB Solutions

For a high power LED aluminum PCB, the useful improvement is a lower-resistance thermal path from the LED into the cooling structure. Increasing the dielectric conductivity can help, but the dielectric thickness, solder interface, copper layout, and heat-sink contact also affect the result.

For the same dielectric thickness and heat-transfer area, a higher-conductivity dielectric reduces that layer's thermal resistance. It does not reduce the entire module's thermal resistance by the same proportion, because the other interfaces remain in the heat path.

Construction Main Advantage Selection Constraint
Aluminum PCB, standard dielectric Balanced cost, weight, and thermal transfer LED heat load and insulation requirements
Aluminum PCB, higher-conductivity dielectric Lower dielectric thermal resistance Material cost, availability, and heat-sink contact
Copper-based or direct-thermal-path construction Suited to concentrated heat sources Cost, weight, isolation, and package compatibility

Copper-based and direct-thermal-path designs require construction-specific electrical-isolation and LED-package review.

Our MCPCB range lets us discuss alternatives when a compact LED array exceeds the practical limits of the proposed aluminum construction. We can review the board structure against the LED package and mounting arrangement before production. Final operating temperature is evaluated in the complete lighting assembly under its intended power and ambient conditions.

Aluminum substrate PCB for lighting supplier

LED PCB Assembly from Bare Boards to Lighting Modules

EBest Circuit provides aluminum PCB fabrication, LED component sourcing, SMT assembly, and agreed board-level testing. We can supply bare boards or assembled LED modules, giving your team one contact for manufacturing and assembly coordination.

  • PCB Fabrication and Assembly: We coordinate pad finish, panel handling, and mounting clearances with the assembly requirements to keep the fabricated board compatible with SMT and integration.
  • LED Sourcing and Binning: We source against the approved manufacturer and part number, including specified color-temperature, luminous-flux, or wavelength bins. Package size alone does not establish optical interchangeability.
  • SMT Process Adaptation: Reflow planning accounts for the aluminum board's thermal mass while respecting component process limits.
  • LED Polarity and Placement: Placement files and assembly drawings define LED orientation and position against the approved optical layout.
  • Testing and Module Delivery: Agreed board-level tests accompany the assembly scope, providing LED boards for the next integration stage. Final luminaire assembly and validation follow the project scope.
Aluminum substrate PCB for lighting supplier

Quality Control for LED Aluminum PCB Production

Quality control needs to protect the features that determine whether the board can be assembled, mounted, and operated as intended. Our manufacturing approach combines material and process control with inspection against the released design.

Electrical Integrity and Insulation: Opens-and-shorts testing verifies circuit continuity and separation; specified dielectric-withstand testing evaluates insulation under defined conditions. Test voltage and procedure must suit the board construction.

Mechanical Fit: Outline dimensions, mounting holes, slots, and finished edges affect fit with the housing or heat sink. Critical drawing dimensions form part of the inspection scope.

Assembly Condition: LED polarity, placement, solder joints, and cleanliness are addressed through agreed inspection and operating tests. Thermal or optical measurements are included when required by the project.

Repeat-Order Control: Approved materials, design revisions, and production records support investigation of variation between deliveries. They also help distinguish similar boards within a lighting product family.

Our Certifications for Aluminum PCB Manufacturing

Our certification portfolio includes ISO 9001:2015, ISO 13485:2016, IATF 16949, and AS9100D. These quality systems support OEM supplier evaluation and provide a structured basis for manufacturing control, traceability, and corrective action.

  • ISO 9001:2015: Quality management covering purchasing controls, process consistency, and customer requirements.
  • ISO 13485:2016: Quality-management support for medical supply chains, including medical-lighting projects within the certified scope.
  • IATF 16949: Automotive quality-management requirements for applicable manufacturing activities and supply chains.
  • AS9100D: Aerospace quality-management requirements for applicable manufacturing and customer programs.

UL, RoHS, and REACH: We support construction-specific UL requirements and product-relevant substance-compliance documentation. These are addressed separately from quality-system certification.

Our quality systems connect manufacturing process control with the documentation needed for customer supplier audits. We align the certificate entity, facility, and scope with the order; finished LED luminaire certification remains specific to the complete product.

Case Study: Custom Aluminum PCB for an LED Lighting Module

Application: A Surgical Lighting Module required an assembled LED board ready for installation in the customer's lighting system.

Manufacturing Challenges: LED positions needed to follow the optical layout, and mounting-hole positions needed to support mechanical fit. The project also required LED operation checks and coordination between board fabrication, component procurement, and assembly.

EBest Circuit Solution: We coordinated custom aluminum PCB fabrication, component sourcing, and SMT assembly under one order. LED placement followed the approved optical layout, critical mounting-hole positions were measured optically, and every LED received an operation check before shipment.

PCB Specifications:

Parameter Specification
Construction Single-sided aluminum PCB
Board Thickness 1.6 mm ±10%
Copper Weight 1 oz
Surface Finish Lead-free HASL
Solder Mask Black
Legend Gray

The customer received fabricated boards, sourced components, and completed SMT assembly in one coordinated delivery. This combined mechanical-fit control and LED assembly verification for the next integration stage.

Why Choose EBest Circuit as Your Aluminum PCB Supplier?

EBest is a strong fit when your lighting project needs custom PCB manufacturing and direct coordination with assembly. Our MCPCB focus dates back to 2006, and our service covers prototypes, production boards, component sourcing, and PCB assembly.

Custom Manufacturing Support: We review copper weight, dielectric construction, board outline, and assembly requirements together. This helps address manufacturing constraints before a compact fixture's mechanical design is released.

One-Stop PCB and Assembly: Fabrication questions are considered alongside the BOM and placement requirements, keeping the board and assembled module aligned within one coordinated project.

Prototype to Production: We support prototypes and production using the agreed construction, with quantities, material availability, assembly scope, and design changes reflected in the quotation.

Production Visibility: One-to-one support and online work-in-progress updates help purchasing and engineering teams track the build and resolve open questions.

MES Production Traceability: For production managed through our MES, we can retrieve linked material, product-batch, and production records in approximately five seconds. This helps OEM teams trace quality issues, manage batches, investigate anomalies, and review manufacturing history for repeat orders.

Certified Quality Management: Our ISO 9001, ISO 13485, IATF 16949, and AS9100D certifications support OEM supplier audits, manufacturing process control, and high-reliability projects within the applicable certified entity, facility, and production scope.

Whether you are launching a new LED module or reviewing an existing supply arrangement, we can quote the manufacturing scope your team needs—from a custom bare board to an assembled lighting PCB.

FAQs About Aluminum Substrate PCB for Lighting

Can I order prototypes before committing to production quantities?

Yes. We support MCPCB prototypes and production builds. A prototype order lets your team evaluate fit, assembly, and operation before releasing the production design.

What quantity should I include when requesting a quotation?

Include the initial build quantity and any expected repeat-order quantities. If your forecast is still developing, we can discuss separate prototype and production pricing rather than assume a fixed annual commitment.

Which files are needed for an aluminum PCB quotation?

For bare boards, send Gerbers, the fabrication specification, mechanical drawing, and quantity. For assembly, add the BOM, placement file, assembly drawing, and required tests. Available files are enough to start a preliminary discussion; the final build uses the agreed manufacturing package.

What affects the price most?

Board area and panel utilization, dielectric material, copper weight, machining, surface finish, and quantity all affect bare-board cost. Assembled-module pricing also includes components, assembly work, and the agreed inspection or testing scope.

Can you quote a replacement for an existing aluminum PCB?

We can review an existing design for manufacture. Gerbers and drawings provide the clearest basis; if only a sample is available, the engineering work needed to establish a production specification must be assessed separately.

How is delivery time determined?

The schedule follows the confirmed board construction, material availability, order quantity, and assembly requirements. For assembled orders, LED and other component availability can influence delivery as much as bare-board fabrication.

Work with an aluminum substrate PCB for lighting supplier that understands both board fabrication and LED assembly. With 20 years of PCB/MCPCB experience, EBest Circuit combines one-stop PCB manufacturing and SMT assembly with DFM engineering support to address manufacturing issues before production. Send your Gerber files, quantity, and technical requirements to sales@bestpcbs.com, and specify whether you need LED assembly. We will prepare a project quotation matched to your board construction and delivery scope.

You may also like

Metal Core PCB for Medical Devices: Applications, Thermal Management & Manufacturing

October 28th, 2026

Metal core PCB for medical devices helps manage heat in surgical lighting, diagnostic equipment, and medical power electronics. Dielectric insulation, thermal resistance, and manufacturing quality remain critical to reliable operation.

EBest Circuit provides custom aluminum and copper core PCB manufacturing, SMT assembly, and free DFM reviews. Its ISO 13485 quality-management certification supports controlled manufacturing for medical-electronics projects within the certificate’s stated entity, site, and scope.

Metal Core PCB for Medical Devices, https://www.bestpcbs.com/blog/2026/10/metal-core-pcb-for-medical-devices/

Which Medical Devices Benefit from Metal Core PCBs?

Metal core PCBs suit medical devices with concentrated heat sources, high-power components, or limited cooling space. They are particularly useful when a conventional FR4 board cannot keep component temperatures within the design limit.

  • Surgical and examination lighting: Aluminum core PCBs transfer heat from high-brightness LED arrays toward the lamp housing or heatsink, helping control LED temperatures during extended operation.
  • Medical phototherapy equipment: Metal substrates spread heat from densely arranged therapeutic LEDs, supporting stable optical output and integration with the equipment’s cooling system.
  • Medical diagnostic equipment: Optical excitation sources and fluorescence detection modules may use MCPCBs to reduce temperature-related instability that can affect measurement consistency.
  • Dental curing and examination devices: Compact high-intensity LED modules benefit from efficient heat transfer where installation space limits conventional cooling options.
  • Medical power electronics: MOSFETs, DC-DC converters, and other power components may use metal substrates when conventional PCB constructions cannot dissipate sufficient heat.

Low-power monitoring, communication, and signal-processing boards may be better suited to FR4, particularly when complex multilayer routing is required.

How Do Metal Core PCBs Improve Thermal Management in Medical Equipment?

Metal core PCBs transfer heat from electronic components through a thermally conductive dielectric into an aluminum or copper substrate. The metal base then spreads heat toward a heatsink, equipment chassis, or another cooling surface.

Metal Core PCB for Medical Devices, https://www.bestpcbs.com/blog/2026/10/metal-core-pcb-for-medical-devices/

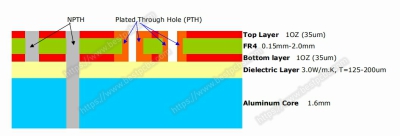
A typical single-sided MCPCB contains a copper circuit layer, an insulating dielectric, and a metal substrate. The dielectric must provide electrical isolation without creating excessive thermal resistance.

Rθ = t / (k × A)

Here, t is dielectric thickness in meters, k is thermal conductivity in W/(m·K), and A is the effective heat-transfer area in square meters.

For example, a dielectric with 100 μm thickness, 2 W/(m·K) thermal conductivity, and an assumed 100 mm² heat-transfer area has a calculated thermal resistance of 0.5 K/W. At a uniform heat flow of 20 W, the estimated temperature difference across that dielectric alone is 10°C.

The actual component temperature also depends on solder joints, component packaging, lateral heat spreading, thermal interface materials, and the cooling system. Medical equipment intended for continuous operation should be evaluated at its maximum expected load, ambient temperature, and duty cycle.

Metal Core PCB vs FR4 for Medical Devices: Which Is Better?

Metal core PCBs are better suited to concentrated heat dissipation, while FR4 offers greater flexibility for complex multilayer circuits and lower-power medical electronics.

Comparison Metal Core PCB FR4 PCB
Base structure Aluminum or copper with insulating dielectric Glass-reinforced epoxy laminate
Thermal management Metal substrate supports efficient heat spreading Relies on copper planes, thermal vias, and external cooling
Electrical insulation Requires a qualified dielectric layer Provided by laminate construction
Circuit complexity Standard IMS is commonly single-sided; complex structures require specialized processing Supports conventional multilayer routing
Mechanical properties Rigid metal substrate provides structural support Available in different thicknesses and constructions
Weight Depends on metal type and thickness Often suitable for lightweight multilayer electronics
Relative cost Usually higher for comparable simple circuits Generally lower for conventional designs
Medical applications LED modules, optical sources, and concentrated power circuits Monitoring, communication, processing, and control boards

An MCPCB becomes practical when an FR4 design cannot meet its thermal limits after considering copper spreading, thermal vias, and improvements to the cooling system.

For medical equipment combining high-power LEDs with complex control circuitry, a separate MCPCB thermal module and FR4 control board may provide a more practical construction.

Aluminum vs Copper Core PCB: Which Is Better for Medical Applications?

Aluminum core PCBs balance thermal performance, weight, and cost, while copper core PCBs offer higher substrate thermal conductivity for concentrated heat sources.

Parameter Aluminum Core PCB Copper Core PCB
Base metal conductivity Approximately 150–230 W/(m·K), depending on alloy and condition Approximately 380–400 W/(m·K), depending on grade and condition
Density Approximately 2.7 g/cm³ Approximately 8.9 g/cm³
Heat spreading Good Higher potential
Weight Lower Higher
Material cost Generally lower Generally higher
Manufacturing Common for standard IMS structures May involve higher material and processing costs
Suitable applications Surgical lighting, examination lamps, and phototherapy modules Compact optical sources and high-heat-flux power modules
Main limitation Lower thermal conductivity Greater weight and cost

For medical LED modules with adequate heatsink contact, aluminum is often a practical starting point. Copper becomes more attractive when heat is concentrated in a small area and the metal substrate limits lateral heat spreading.

If dielectric resistance or heatsink contact dominates the thermal path, replacing aluminum with copper may produce only a limited temperature reduction.

What Technical Specifications Matter for Medical Metal Core PCBs?

For a metal core PCB for medical devices, the critical specifications are dielectric thermal performance, electrical insulation, circuit copper thickness, substrate thickness, and mechanical tolerances.

Specification Typical Design Reference Selection or Acceptance Criteria
Base material Aluminum or copper Thermal load, weight, and cost
Dielectric conductivity Common grades around 1–3 W/(m·K) Approved material datasheet and thermal requirements
Dielectric thickness Often 75–150 μm Thermal resistance and insulation performance
Circuit copper Common options of 1–3 oz Current capacity, trace geometry, and heat distribution
Finished thickness Often approximately 0.8–3.0 mm Mechanical fit and mounting requirements
Surface finish ENIG, OSP, lead-free HASL, or another qualified finish Solderability and assembly compatibility
Dielectric withstand Project-specific Test method, voltage, duration, and acceptance limit
Board flatness Drawing-specific Heatsink contact and mounting alignment
Operating temperature Application-specific Component limits and material ratings

Dielectric selection requires balancing conductivity, thickness, and insulation performance. A thinner dielectric generally reduces thermal resistance, but it must still satisfy the required electrical-insulation conditions.

Electrical insulation should be specified through measurable requirements, including the approved dielectric material, test voltage, duration, and acceptance criteria. Required creepage and clearance depend on the equipment’s electrical-safety design.

Mechanical requirements should define mounting-hole positions, critical dimensions, flatness, and the heatsink interface. Thermal acceptance criteria should identify operating power, ambient temperature, measurement location, stabilization conditions, and the maximum allowable component temperature.

How Can Engineers Avoid Thermal and Insulation Failures in Medical MCPCB Design?

The main failure risks in medical MCPCB designs are localized overheating, damaged insulation, poor heatsink contact, and thermal-expansion stress. These problems may develop during extended operation even when initial electrical testing is successful.

  • Local hot spots: Review component power loss, thermal-pad dimensions, solder attachment, and heat spreading. High temperatures near a component can indicate restrictions in the local thermal path.
  • Dielectric breakdown: Check insulation thickness and electrical clearance around circuit features, metal edges, and mounting holes. Exposed metal or drilling damage may create unintended conductive paths.
  • Poor heatsink contact: Inspect mounting flatness, thermal-interface material, fastening pressure, and contact area. Air gaps can increase thermal resistance.
  • Thermal-cycling stress: Account for differences in expansion among the metal base, dielectric, solder joints, and components. Repeated temperature changes can contribute to solder fatigue or interfacial damage.
  • Temperature-sensitive components: Position sensitive analog circuitry and sensors away from significant heat sources where practical because metal substrates can spread heat into nearby regions.

When investigating overheating, compare component temperature, local metal-base temperature, and heatsink temperature to locate the dominant thermal resistance. A large difference between the metal base and heatsink may indicate poor contact, while excessive component temperature relative to the nearby metal base may point to component attachment or local heat-transfer limits.

How Are Metal Core PCBs for Medical Devices Manufactured and Assembled?

Medical metal core PCB production combines substrate preparation, circuit fabrication, metal machining, surface finishing, and SMT assembly. The process must maintain dielectric insulation, mechanical accuracy, and reliable solder joints.

PCB Manufacturing Process

  1. Select and verify materials: Start from the approved stackup and select the aluminum or copper substrate, thermally conductive dielectric, and circuit copper. Verify material identity, thickness, dielectric properties, and surface condition so an incorrect laminate does not enter imaging.
  2. Image and etch the circuit: Apply photoresist, expose and develop the circuit pattern, and etch unwanted copper. Inspect conductor dimensions and spacing against the released fabrication data before metal machining can hide or compound an imaging error.
  3. Drill and route the metal panel: Machine mounting holes, slots, and board outlines with suitable tooling. Check dimensions, metal burrs, exposed edges, and dielectric condition because machining damage can reduce clearance or create an unintended conductive path.
  4. Apply solder mask and surface finish: Process the specified solder mask and finish, such as ENIG, OSP, or lead-free HASL. Verify mask registration and pad condition so the assembly surface matches the released finish and solderability requirements.
  5. Inspect and electrically test the PCB: Verify continuity, isolation, board dimensions, and critical mounting features against the drawing. Release the bare board only when the recorded results meet the order’s acceptance criteria.

PCB Assembly Process

  1. Print and inspect solder paste: Apply paste through the approved stencil and use SPI when included in the agreed inspection plan. Evaluate deposit volume, alignment, and printing defects before component placement.
  2. Place and verify components: Mount LEDs, power devices, resistors, and other components with SMT equipment. Check orientation, placement accuracy, and thermal-pad alignment against the assembly data before reflow.
  3. Profile and run reflow: Develop a temperature profile suited to the metal substrate’s thermal mass, solder paste, and component limits. Use thermocouples at representative locations to confirm adequate joint formation without excessive component heating.
  4. Inspect the assembled board: Use AOI for placement and visible solder joints. Add X-ray inspection for hidden connections or solder-voiding criteria only when the package, thermal pad, and agreed inspection scope require it.
  5. Run agreed tests and protect shipment: Perform the specified electrical or functional tests, record the applicable result, and package completed assemblies to prevent mechanical or ESD damage in transit.

What Quality Tests and Certifications Should Medical MCPCB Manufacturers Provide?

Medical MCPCB suppliers should provide electrical-test results, insulation verification, dimensional records, and the quality-system evidence required by the order. The exact evidence depends on the PCB construction, assembly scope, and medical-equipment requirements.

Metal Core PCB for Medical Devices, https://www.bestpcbs.com/blog/2026/10/metal-core-pcb-for-medical-devices/

Quality Tests

  • Electrical testing: Verifies circuit continuity and isolation to identify open circuits, shorts, and unintended electrical connections.
  • Dielectric withstand and insulation resistance: Confirms insulation performance under specified electrical conditions. Records should include the method, voltage, duration, acceptance limits, and measured results where applicable.
  • Dimensional inspection: Checks board thickness, outline, mounting holes, and critical dimensions against the approved fabrication drawing.
  • AOI, SPI, and X-ray inspection: Detect relevant manufacturing and assembly defects. SPI assesses solder-paste deposits, AOI identifies visible defects, and X-ray supports inspection of hidden solder joints where required.
  • Thermal and functional testing: Evaluates component temperatures, hot spots, or specified circuit functions under defined operating conditions. Thermal cycling or other reliability tests may be added when required by the qualification plan.
  • Material traceability: Links the manufactured PCB to its approved substrate, dielectric material, production lot, and relevant inspection records.

Certifications and Standards

  • ISO 13485:2016: Defines quality-management-system requirements for organizations involved in medical devices and related services. Buyers should verify the certificate’s entity, site, scope, and validity.
  • ISO 9001: Provides general quality-management-system requirements. ISO 9001:2026 is the current edition; buyers should also check the supplier’s certificate version and transition status.
  • IPC-A-600: Provides acceptability criteria for bare printed boards. The applicable revision and product class should be stated in the purchasing documents.
  • IPC-A-610: Provides acceptability criteria for electronic assemblies. The applicable revision and class should match the assembly contract.
  • IEC 60601-1: Covers general requirements for basic safety and essential performance of applicable medical electrical equipment and systems; collateral or particular standards may also apply.

An ISO 13485 certificate applies to the certified quality-management system and scope, not to an individual PCB product. IEC 60601-1 requirements are assessed at the equipment level. Buyers should verify certificate validity, manufacturing-site coverage, the applicable standards and revisions, and the inspection documents included with the order.

Why Choose EBest Circuit for Medical Metal Core PCB Manufacturing?

EBest Circuit combines custom metal core PCB fabrication, component sourcing, SMT assembly, and engineering support for medical-electronics manufacturers. Each capability should be confirmed against the released stackup, files, inspection scope, and certificate requirements for the project.

  • ISO 13485 and ISO 9001 certification: Supports controlled manufacturing, documentation, and production traceability within the applicable certificate entity, site, scope, and validity period.
  • Free DFM review: Engineers can check dielectric specifications, copper features, mounting-hole insulation, mechanical dimensions, and assembly files to identify manufacturability issues before fabrication.
  • Aluminum and copper core options: Published capability references cover single-sided, double-sided, and selected multilayer constructions, plus dielectric grades of 0.8, 1.0, 1.5, 2.0, and 3.0 W/(m·K). Final material and construction suitability are confirmed for each project.
  • Integrated PCB and PCBA workflow: Fabrication, component sourcing, SMT assembly, and agreed inspection can be coordinated under one project to reduce supplier handoffs.
  • Prototype-to-volume support: Approved stackups, materials, BOMs, and inspection requirements can be controlled across repeat orders to support manufacturing consistency.
  • Defined testing and documentation: Electrical testing, SPI, AOI, applicable X-ray inspection, and customer-defined functional or thermal testing are quoted only within the confirmed production scope.
  • International delivery support: Customized PCB and PCBA manufacturing is coordinated from China-based operations for overseas medical-electronics customers.

Medical Metal Core PCB Application Case: Improving Thermal Stability in a Diagnostic Device

An EBest customer project used a copper-base PCB to improve the thermal stability of a compact optical-detection module without increasing its enclosure size. The project result was evaluated at prototype level before moving into small-batch production.

Project Background

A medical diagnostic equipment manufacturer experienced unstable optical readings in a compact laboratory detection module. The original FR4 PCB passed initial functional testing, but prolonged operation caused heat to accumulate around the LED excitation source, resulting in brightness drift and inconsistent signal output.

Customer Requirements and Challenges

The customer needed better thermal stability without increasing the module size. The replacement PCB also had to maintain electrical insulation, reliable LED soldering, and accurate mechanical fit with the existing enclosure. The main challenge was reducing heat buildup while preserving the optical and assembly requirements.

EBest Circuit’s Solution

EBest reviewed the LED thermal pads, copper distribution, dielectric material, substrate thickness, and enclosure contact points. The engineering team replaced the FR4 construction with a copper-base PCB, enlarged the thermal-pad area, selected a higher-conductivity dielectric, and improved the heat-transfer interface with the metal enclosure. Thermal imaging was included in prototype evaluation to assess heat distribution during operation.

Project Results

The revised prototype reduced localized hot spots and improved LED output stability during continuous operation. The customer obtained a more stable optical module without increasing its dimensions. Following prototype verification, the project advanced to small-batch production with defined material specifications and inspection requirements for subsequent orders.

FAQs About Metal Core PCBs for Medical Devices

Q1. Can a metal core PCB use plated through-holes?

A1. Yes, certain MCPCB constructions support plated through-holes, but they require suitable insulation and specialized processing. Manufacturability depends on the stackup, metal thickness, and electrical-isolation requirements.

Q2. Is the aluminum or copper substrate connected to ground?

A2. Not automatically. The metal base may be electrically isolated or intentionally connected through a designed grounding structure. Grounding and isolation must be defined in the equipment design, especially around mounting screws and exposed metal.

Q3. Can medical MCPCBs support double-sided component assembly?

A3. Some double-sided and multilayer MCPCB constructions support components on both surfaces. The required interconnections, insulation, and assembly processes are more complex, so the complete stackup must be reviewed before manufacturing.

Q4. Are metal core PCBs suitable for portable medical equipment?

A4. Yes, especially when a compact power or LED module generates concentrated heat. Aluminum may provide a suitable balance of thermal performance and weight, depending on board thickness and mechanical requirements.

Q5. Can medical MCPCBs withstand sterilization?

A5. Compatibility depends on the sterilization process and the complete assembly. Steam, moisture, chemicals, and repeated heating can affect dielectric materials, solder joints, and components. The assembly must be qualified for the intended sterilization method.

Q6. Can damaged components be reworked on a metal core PCB?

A6. Rework may be possible, but the metal base changes heat distribution around the repair area. A qualified rework profile and temperature monitoring help reduce the risk of component or dielectric damage.

Q7. Are MCPCBs suitable for disposable medical equipment?

A7. They may be appropriate for disposable products containing significant heat sources. Power density, operating duration, weight, and cost should determine whether a metal substrate is justified.

Q8. Can an MCPCB eliminate the need for a separate heatsink?

A8. Sometimes, but not automatically. The metal substrate spreads heat, while the surrounding structure must release it to the environment. Heatsink removal requires thermal verification under the intended operating conditions.

Q9. What affects the lead time for custom medical metal core PCBs?

A9. Lead time depends on substrate availability, dielectric requirements, circuit complexity, machining, quantity, assembly, and testing. A production schedule should be confirmed after engineering and material review.

How Can You Get a Medical Metal Core PCB Quote?

A useful medical MCPCB quotation starts with released fabrication data, thermal and insulation requirements, assembly files, and the required inspection records. EBest Circuit can review the following inputs for a manufacturing and assembly quotation:

  • PCB files: Gerber or ODB++ data, drill files, mechanical drawings, and stackup.
  • Material specifications: Aluminum or copper substrate, dielectric requirements, copper thickness, board thickness, and surface finish.
  • Thermal and electrical requirements: Power dissipation, operating temperature, insulation specifications, and acceptance criteria.
  • Assembly information: BOM, pick-and-place files, assembly drawings, and required functional tests.
  • Quality requirements: Applicable IPC acceptance class, inspection requirements, and traceability documents.
  • Order details: Prototype or production quantity, target delivery date, and delivery location.

The returned engineering review can identify manufacturing-feasibility questions and the material, insulation, assembly, test, or documentation choices that affect the quotation and production schedule.

For a free DFM review and custom medical metal core PCB quotation, send the released files and requirements to sales@bestpcbs.com.

You may also like

Metal Core PCB for Automotive Electronics: From Design to Production

October 28th, 2026

Metal core PCB for automotive electronics is commonly used in LED headlights, daytime running lights, and selected power control modules where concentrated heat must be transferred to a vehicle housing or heat sink. Compared with conventional FR4, metal-backed PCBs offer an effective way to manage heat in compact automotive assemblies.

However, thermal conductivity alone does not guarantee reliable performance. Dielectric insulation, component placement, mounting conditions, and manufacturing consistency determine how well an MCPCB performs under automotive operating conditions. Selecting the right materials and validating the complete assembly can prevent overheating, insulation failures, and costly production changes.

metal core PCB for automotive electronics, https://www.bestpcbs.com/blog/2026/10/metal-core-pcb-for-automotive-electronics/

Which Automotive Electronics Applications Benefit Most from Metal Core PCBs?

Metal core PCBs are particularly suitable for automotive lighting and selected power electronics with concentrated heat sources. Common applications include:

  • LED Headlights: Transfer heat from high-power LED arrays to the headlamp heat sink, helping maintain acceptable junction temperatures in compact housings.
  • Daytime Running Lights (DRLs): Improve heat transfer during continuous LED operation, particularly where airflow and installation space are limited.
  • Brake and Tail Lights: Spread heat generated by LED clusters, reducing localized temperature buildup in enclosed lighting modules.
  • Automotive Infrared Illumination: Manage heat from high-output IR LEDs used in selected driver monitoring and sensing systems.
  • Auxiliary Power Converters: Provide a thermal path for MOSFETs, rectifiers, and voltage regulators when the circuit and mounting structure suit a metal-backed substrate.
  • Motor Driver Modules: Help transfer heat from power transistors into a motor housing or external cooling structure.

Not every automotive electronic system benefits from a metal core PCB. Complex ECUs, BMS control boards, and ADAS processors often use multilayer FR4 or specialized substrates to accommodate dense circuitry and high-speed signals.

Metal Core PCB vs. FR4 vs. Ceramic PCB: Which Is Right for Automotive Electronics?

The choice between metal core PCB, FR4, and ceramic PCB depends on heat load, circuit complexity, electrical isolation, mounting requirements, and manufacturing cost.

Comparison Metal Core PCB FR4 PCB Ceramic PCB
Thermal performance Metal base spreads heat toward a cooling surface Lower through-thickness thermal conductivity; additional thermal structures may be required High thermal conductivity with suitable ceramic materials
Electrical insulation Provided by the dielectric layer Provided by resin-glass laminate Common ceramic substrates are electrically insulating
Circuit complexity Conventional IMS favors simpler routing; specialized multilayer options available Suitable for complex multilayer routing Depends on ceramic manufacturing technology
Weight Aluminum is relatively light; copper is heavier Generally lightweight Depends on material and construction
Mechanical properties Rigid metal-backed structure Versatile mechanical characteristics Hard and dimensionally stable but brittle
Cost Moderate for conventional aluminum IMS Generally economical for standard designs Often higher for specialized structures
Typical applications Automotive lighting and selected power modules ECU, BMS control, infotainment Specialized power modules and semiconductor packaging
Main limitation Dielectric thermal resistance and routing restrictions Heat removal from concentrated power devices Brittleness and manufacturing complexity

What Are the Key Design Requirements for Automotive Metal Core PCBs?

Automotive metal core PCB design begins with the conditions the finished module will face in service. Operating temperature, power dissipation, electrical isolation, and mechanical installation directly affect material selection and PCB construction.

The main design requirements include:

  • Operating Temperature: Define minimum and maximum ambient temperatures, expected enclosure temperature, and operating duty cycle.
  • Power Dissipation: Calculate the heat produced by LEDs, MOSFETs, regulators, and other power components under maximum operating loads.
  • Electrical Isolation: Specify working voltage, dielectric withstand requirements, creepage, clearance, and grounding arrangements.
  • Current Capacity: Determine conductor dimensions and copper thickness based on current loading and allowable temperature rise.
  • Mechanical Installation: Confirm PCB dimensions, mounting holes, flatness, fastening positions, and heat-sink contact requirements.
  • Environmental Conditions: Account for temperature cycling, vibration, humidity, contamination, and other service conditions.

An LED headlight inside a sealed housing, for example, may operate at a much higher temperature than the surrounding air. A PCB designed using only room-temperature measurements can underestimate the thermal stress experienced during vehicle operation.

Worst-case operating conditions should govern the final design, particularly when power devices have limited junction-temperature margins.

How Do You Select the Right Metal Core PCB Materials and Stackup?

An automotive metal core PCB typically consists of copper circuitry, a thermally conductive dielectric layer, and an aluminum or copper base. The copper carries electrical current, the dielectric provides insulation, and the metal base spreads heat toward the cooling structure.

Aluminum is widely used in automotive lighting because it offers useful heat spreading with relatively low weight and cost. Copper has higher bulk thermal conductivity but adds weight and expense, making it more suitable where its additional thermal performance is justified.

Design Parameter Selection Consideration Verification
Metal base Aluminum for weight and cost balance; copper where higher conductivity offers an advantage Material grade, thickness and housing compatibility
Dielectric conductivity Higher conductivity can reduce resistance through the insulating layer Material datasheet and thermal properties
Dielectric thickness Thinner layers reduce thermal resistance but may affect insulation margins Thickness, dielectric withstand and aging performance
Copper thickness Depends on current, conductor geometry and temperature rise Current-capacity calculation and fabrication limits
Base thickness Affects stiffness, weight, machining and mounting compatibility Mechanical drawing and installation requirements
Surface finish ENIG, lead-free HASL or OSP based on assembly requirements Solderability, component compatibility and planarity
Stackup structure Single-sided IMS or specialized multilayer construction Routing, isolation and manufacturing feasibility

The dielectric is often the most critical material choice. A material with 2.0 W/m·K thermal conductivity can provide useful heat transfer, but its resistance also depends on thickness and effective heat-transfer area.

The insulation system must retain suitable electrical and mechanical properties under the specified automotive environment. Thermal conductivity, dielectric strength, aging resistance, and processing compatibility should be evaluated together.

How Do You Calculate and Optimize Thermal Performance in Automotive MCPCB Design?

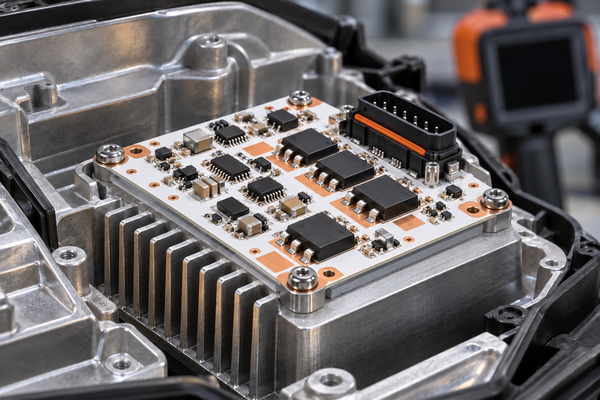
Automotive MCPCB thermal performance depends on the entire path from the component junction to the surrounding environment. Heat passes through the component package, solder connection, copper circuitry, dielectric layer, metal base, thermal interface material, and heat sink or housing.

metal core PCB for automotive electronics, https://www.bestpcbs.com/blog/2026/10/metal-core-pcb-for-automotive-electronics/

The maximum allowable junction-to-ambient thermal resistance can be estimated using:

RθJA,max = (TJ,max − TA) / P

Where:

  • TJ,max: Maximum permitted junction temperature
  • TA: Ambient temperature
  • P: Component power dissipation
  • RθJA,max: Maximum allowable junction-to-ambient thermal resistance

Consider a power device dissipating 8 W at an ambient temperature of 85°C, with a selected junction-temperature design limit of 125°C.

The allowable thermal resistance is:

RθJA,max = (125 − 85) / 8 = 5°C/W

The complete assembly must therefore maintain an effective thermal resistance of 5°C/W or less under these assumed conditions.

The dielectric layer contributes to this resistance. Its idealized through-thickness resistance can be estimated as:

Rθ = t / (k × A)

Here, t is dielectric thickness, k is thermal conductivity, and A is the effective heat-transfer area.

For a 100 µm dielectric, 2 W/m·K conductivity, and an assumed heat-transfer area of 100 mm², the calculated resistance is 0.5°C/W. This excludes spreading resistance, contact resistance, and other heat-transfer losses.

Thermal improvements should concentrate on:

  • Component Placement: Position high-power devices where heat can reach the cooling surface through a short thermal path.
  • Copper Distribution: Provide sufficient conductor area for current handling and heat spreading.
  • Dielectric Selection: Balance thermal conductivity, layer thickness, and electrical insulation.
  • Thermal Interface: Control mounting pressure, board flatness, and thermal interface material thickness.
  • Temperature Verification: Measure component and PCB temperatures under representative power loads and enclosure conditions.

For assemblies containing several power devices, simultaneous heat generation must be included in the thermal assessment. A calculation establishes the initial target, while measurements on the assembled module confirm whether that target has been met.

How Can You Prevent Common Automotive Metal Core PCB Design and Assembly Failures?

Automotive MCPCB failures often develop around solder joints, dielectric interfaces, and mechanical mounting points. Repeated temperature changes produce expansion differences between materials, while vibration and mounting stress can damage electrical connections over time.

Common failure risks include:

  • Solder Joint Cracking: Thermal expansion mismatch and vibration can fatigue solder joints. Suitable pad geometry, component support, and mounting arrangements help reduce mechanical stress.
  • Dielectric Breakdown: Insufficient insulation margins, material defects, or machining damage can compromise electrical isolation. Proper dielectric selection and clearance control are essential.
  • Delamination: Excessive thermal stress or incompatible materials can weaken bonded layers. Qualified laminates and controlled fabrication conditions reduce this risk.
  • Board Deformation: Uneven fastening pressure can distort the assembly or reduce contact with the heat sink. Mounting-hole placement and board flatness require attention.
  • Solder Voiding: Inappropriate solder paste deposition or reflow conditions can weaken solder connections. Stencil design and soldering profiles should be validated for the actual substrate.
  • Moisture-Related Leakage: Contamination and environmental exposure can reduce insulation resistance. Cleanliness controls and suitable protective materials help maintain electrical performance.

Mounting details are particularly important in metal-backed assemblies. Exposed metal edges and fasteners must not create unintended electrical paths, while excessive clamping force can damage solder joints or compromise the thermal interface.

How Are Automotive Metal Core PCBs Manufactured and Assembled?

Automotive metal core PCB production involves PCB fabrication and component assembly. Both stages require controlled processing to maintain electrical insulation, thermal performance, and dimensional accuracy.

PCB Manufacturing Process

  1. Material Preparation: Inspect the aluminum or copper-backed laminate, dielectric layer, and copper foil to confirm material specifications, thickness, and surface condition.
  2. Circuit Patterning and Etching: Form copper circuits through imaging and chemical etching while maintaining conductor dimensions, spacing, and dielectric integrity.
  3. Solder Mask and Surface Finishing: Apply the specified solder mask and surface finish, such as ENIG or lead-free HASL, to protect exposed circuitry and provide solderable surfaces.
  4. Mechanical Processing: Produce the board outline, mounting holes, and required cutouts. Control metal burrs, dimensional tolerances, and insulation clearance around exposed edges.
  5. Bare PCB Inspection: Perform electrical testing, dimensional checks, and visual inspection to verify circuit integrity and fabrication quality.

PCB Assembly Process

  1. Solder Paste Printing: Apply solder paste to component pads using a suitable stencil, controlling deposition volume and alignment.
  2. Component Placement: Mount LEDs, MOSFETs, resistors, and other components according to the approved BOM and placement data.
  3. Reflow Soldering: Use a validated temperature profile that accounts for the metal substrate’s thermal characteristics and component soldering requirements.
  4. Assembly Inspection: Inspect component alignment and solder joints using AOI, visual inspection, and X-ray where appropriate.
  5. Functional and Thermal Testing: Verify electrical operation and, where required, measure component temperatures under defined power loads.

The finished PCB must also meet the mounting dimensions and contact requirements of the automotive housing, particularly when the metal base forms part of the assembly’s cooling path.

What Tests Verify Automotive Metal Core PCB Quality and Reliability?

Automotive metal core PCB testing covers electrical integrity, insulation performance, fabrication quality, and assembly reliability. Test requirements depend on the product specification and customer qualification plan.

metal core PCB for automotive electronics, https://www.bestpcbs.com/blog/2026/10/metal-core-pcb-for-automotive-electronics/
  • Electrical Continuity Testing: Detect open circuits and unintended electrical connections in finished bare PCBs.
  • Dielectric Withstand Testing: Verify that the insulation withstands the specified test voltage without electrical breakdown.
  • Insulation Resistance Testing: Measure electrical leakage between isolated conductive structures under defined conditions.
  • Dimensional and Visual Inspection: Check PCB thickness, mounting holes, edge quality, solder mask, and visible manufacturing defects.
  • Solder Joint Inspection: Use AOI, visual inspection, or X-ray as appropriate to identify soldering defects and placement problems.
  • Thermal Performance Testing: Measure LED or semiconductor temperatures under specified electrical loads and cooling conditions.
  • Temperature Cycling Testing: Evaluate solder joint integrity, material interfaces, and insulation reliability after repeated temperature changes.
  • Vibration Testing: Assess mechanical durability and electrical connection stability under the required automotive vibration profile.
  • Functional Testing: Confirm that the assembled circuit meets its electrical and operating specifications.

PCB quality requirements may reference IPC-6012F, IPC-6012FA, and IPC-A-600, while assembly acceptance may follow IPC J-STD-001 and IPC-A-610. The applicable standards and acceptance criteria should be established for the project.

Temperature cycling, vibration, and other environmental qualification tests follow the customer’s approved test plan rather than being performed automatically on every production board.

How Do You Move Automotive Metal Core PCBs from Prototype to Volume Production?

Moving an automotive metal core PCB into volume production requires repeatable manufacturing results, not simply a larger order quantity. The approved design, materials, and inspection requirements must remain consistent as production increases.

Engineering Prototypes

Initial samples verify PCB dimensions, electrical isolation, component assembly, mounting fit, and thermal performance. Any design changes identified during testing are incorporated into controlled manufacturing revisions before the next build.

Pilot Production

A representative production run evaluates process stability. Particular attention is given to dielectric integrity, machining accuracy, solder joint quality, and inspection consistency. Problems discovered at this stage should be resolved before full production release.

Volume Production

Approved materials, manufacturing files, inspection criteria, and process requirements are maintained throughout production. Depending on customer requirements, automotive programs may involve APQP, PPAP, PFMEA, control plans, and production part approval documentation.

Material lot identification, inspection records, and revision control help maintain consistency between batches. Changes involving approved materials or manufacturing processes may require customer notification and additional validation.

Automotive Metal Core PCB Case Study: From Engineering Requirements to Production

Project Background

EBest Circuit manufactured an aluminum-based metal core PCB for an automotive LED headlamp application. The project required a compact board with effective heat transfer, electrical insulation, and a solderable surface suitable for the lighting assembly.

Requirements and Challenges

The customer specified a 1.5 mm board thickness, 3 oz copper, a 2.0 W/m·K thermal conductivity rating, white solder mask, ENIG surface finish, and 100% electrical testing. The main challenge was combining a metal-backed construction with relatively heavy copper circuitry while maintaining the required board dimensions and electrical isolation.

EBest Circuit Solution

EBest Circuit manufactured the aluminum-backed PCB with the specified copper thickness, insulation structure, solder mask, and surface finish. The 3 oz copper supported the required conductor construction, while ENIG provided a planar solderable finish for component assembly. White solder mask was selected for the lighting application, where visible-light reflection can be beneficial. Fabrication and inspection were arranged around the specified board structure and electrical testing requirements.

Project Results

The project was manufactured using the specified metal-backed construction, with 100% electrical testing included in the production requirements. The resulting PCB provided the required construction for the automotive lighting application, including heavy copper circuitry, a solderable surface, and an electrically insulated metal base.

How Should You Evaluate an Automotive Metal Core PCB Manufacturer?

A reliable automotive metal core PCB manufacturer should be able to demonstrate suitable manufacturing capabilities, controlled production processes, and relevant quality documentation.

Before selecting a supplier, engineering and purchasing teams should evaluate:

  • Manufacturing Capability: Confirm available metal substrates, dielectric systems, copper thicknesses, PCB structures, and machining tolerances.
  • Quality Certification: Verify ISO 9001 or IATF 16949 certificates, including certificate validity, the certified facility, and applicable scope.
  • Material Traceability: Request laminate specifications, material identification, lot records, and relevant conformity documentation.
  • Engineering Support: Check whether the manufacturer provides practical DFM feedback on electrical insulation, mounting features, material choices, and assembly limitations.
  • Testing Capability: Confirm available electrical, dielectric, dimensional, and assembly inspection methods.
  • Production Control: Evaluate revision management, process qualification, corrective actions, and customer approval procedures.
  • Commercial Reliability: Compare quotation coverage, material availability, tooling costs, production lead time, and delivery conditions.

For automotive OEM and Tier 1 programs, supplier audits and customer-specific production approval requirements may also apply.

Why Choose EBest Circuit for Automotive Metal Core PCB Manufacturing?

EBest Circuit provides custom metal core PCB manufacturing and assembly services for automotive lighting and selected power electronics applications. Our China-based manufacturing operations support customers from engineering prototypes through repeat production.

Customers can benefit from:

  • IATF 16949 and ISO 9001 Quality Management: Quality management certifications supporting controlled manufacturing and automotive project requirements. Relevant certification documentation can be provided for customer review.
  • Free DFM Review: Engineering feedback on fabrication constraints, dielectric insulation, mounting features, material selection, and assembly feasibility before production.
  • Custom Metal Core PCB Manufacturing: Aluminum and copper-based solutions with materials, copper thicknesses, surface finishes, and mechanical features selected according to project requirements.
  • One-Stop PCB Fabrication and Assembly: Coordinated PCB manufacturing, component sourcing, SMT assembly, and applicable inspection services.
  • Prototype and Volume Production: Support for engineering samples, pilot builds, and repeat manufacturing orders with controlled revisions.
  • Engineering and Quality Support: Assistance with technical specifications, material documentation, manufacturing questions, and agreed inspection requirements.

For automotive electronics projects, a free DFM review can identify fabrication and assembly risks before tooling and production begin, helping customers avoid unnecessary revisions and delays.

FAQs About Metal Core PCB for Automotive Electronics

Q1: Is the aluminum base of an automotive MCPCB electrically grounded?

A1: Not automatically. The metal base is insulated from the circuit copper. Chassis grounding requires an intentional electrical connection through the approved mounting design.

Q2: Can automotive metal core PCBs support plated-through holes?

A2: Yes, with suitable specialized constructions. Conventional single-sided IMS has limitations, and holes passing through the metal base require proper electrical isolation.

Q3: Can components be mounted on both sides of a metal core PCB?

A3: Yes, depending on the construction. Standard single-sided IMS typically supports components on one side, while specialized multilayer structures can accommodate more complex assemblies.

Q4: Why is white solder mask used in automotive LED PCBs?

A4: White solder mask can improve visible-light reflection in LED modules. Reflectivity, thermal stability, and resistance to discoloration should guide material selection.

Q5: Can automotive MCPCBs use lead-free solder?

A5: Yes. Lead-free SMT assembly is possible with compatible materials and components. Reflow profiles must be validated because the metal substrate affects heating behavior.

Q6: Does a metal core PCB eliminate the need for a heat sink?

A6: Not necessarily. The metal base spreads heat, but high-power devices may still require an external heat sink or metal housing. Total thermal resistance determines cooling requirements.

Q7: Can conformal coating protect automotive MCPCBs from moisture?

A7: Yes. Suitable conformal coatings help protect assembled circuitry from moisture and contamination. Coating must not interfere with electrical contacts or thermal interfaces.

Q8: Are halogen-free MCPCB materials automatically RoHS compliant?

A8: No. Halogen-free specifications and RoHS requirements address different chemical restrictions. Separate compliance documentation may be required.

Q9: Can press-fit connectors be installed on automotive MCPCBs?

A9: Only when the PCB construction supports the required hole structure and insertion forces. Conventional IMS may not support standard press-fit connections without specialized construction.

Q10: What packaging protects automotive metal core PCBs during shipping?

A10: Protective trays, separators, and suitable cushioning help prevent surface damage, edge defects, and component damage. Packaging and lot identification should match the customer’s requirements.

How Can You Get a Custom Automotive Metal Core PCB Quote?

EBest Circuit provides custom metal core PCB fabrication and optional assembly services for automotive electronics projects. Quotations are based on the board construction, technical requirements, testing scope, and order quantity.

For an accurate quotation, please provide:

  • PCB Files: Gerber data, drill files, mechanical drawings, and stackup requirements.
  • Material Specifications: Aluminum or copper base, dielectric properties, copper thickness, board thickness, and surface finish.
  • Operating Requirements: Power dissipation, temperature range, electrical isolation, mounting conditions, and applicable automotive standards.
  • Assembly Information: BOM, component placement files, assembly drawings, and required testing.
  • Order Details: Quantity, required delivery date, and delivery location.
  • Quality Requirements: Inspection criteria, traceability expectations, and customer-specific approval documentation.

Planning a metal core PCB for automotive electronics project? Whether you are developing prototypes or preparing for volume production, EBest Circuit can help you review material specifications, verify manufacturing feasibility, and coordinate PCB fabrication and assembly. Send your project files and requirements to sales@bestpcbs.com for a free DFM review, engineering support, and a custom quotation.

You may also like

Multilayer PCB Manufacturing for Telecom Systems

October 23rd, 2026

EBest Circuit provides multilayer PCB manufacturing for telecom systems, supporting standard 1–10 layer FR-4 PCBs and special multilayer constructions up to 32 layers. Our capabilities include controlled impedance, HDI structures, high-frequency materials, PCB prototyping, and turnkey assembly.

For 5G base stations, network switches, routers, and optical communication equipment, we provide custom fabrication, DFM review, component sourcing, and PCBA services. Send your specifications to sales@bestpcbs.com for a manufacturing feasibility review and quotation.

multilayer PCB manufacturing for telecom systems, https://www.bestpcbs.com/blog/2026/10/multilayer-pcb-manufacturing-for-telecom-systems/

Why Choose Multilayer PCBs for Telecom Systems?

Multilayer PCBs provide the routing density, dedicated reference planes, and power distribution needed for complex telecom equipment. They accommodate high-speed interfaces, RF circuits, and dense components while keeping board dimensions manageable.

Telecom Equipment Why Multilayer PCBs Are Used Main Requirements
5G Base Stations Integrate RF, digital control, and power circuits Controlled impedance, suitable RF materials, thermal reliability
Network Switches Support dense components and high-speed data channels Low-loss signal paths, reliable vias, stable stackups
Routers and Gateways Combine processors, memory, and communication interfaces Compact construction, EMI control, continuous reference planes
Optical Communication Equipment Connect optical transceivers to high-speed digital circuits Signal integrity, connector accuracy, dielectric stability
Telecom Power and Control Boards Separate control, monitoring, and power distribution Copper thickness, thermal management, electrical insulation

More layers do not automatically improve performance. The appropriate layer count depends on routing density, operating conditions, component packages, and electrical requirements. For high-speed and RF applications, laminate properties and stackup construction also influence signal performance.

What Are EBest Circuit’s Multilayer PCB Manufacturing Capabilities?

EBest Circuit supports multilayer PCB fabrication up to 32 layers, including fine-line circuits, high-density interconnections, heavy copper, and special laminate constructions.

Manufacturing Parameter Standard Capability Special Process Capability
PCB Layer Count 1–10 layers 10–32 layers
Minimum Line Width / Spacing at 1 oz Copper 4/4 mil 3/3 mil
Minimum Finished Mechanical Hole 0.20 mm 0.15 mm
Minimum Laser Blind Via Diameter 0.10 mm Special HDI structures require review
Inner-Layer Copper Thickness 0.5–5 oz Up to 20 oz
Outer-Layer Copper Thickness 1–5 oz Up to 20 oz
PTH Hole Diameter Tolerance ±3 mil ±2 mil
NPTH Hole Diameter Tolerance ±2 mil ±1 mil
Surface Finishes HASL, OSP, ENIG, immersion silver/tin ENEPIG, hard gold, and other specified finishes

Manufacturing limits depend on the complete PCB construction. Fine-line capabilities vary with copper thickness, while finished hole diameter, aspect ratio, material properties, and board thickness determine whether a multilayer stackup can be manufactured.

For example, a 16-layer telecom PCB combining heavy copper and fine-pitch signal routing requires separate evaluation of the copper distribution, lamination structure, and drilling requirements.

EBest Circuit supports the following specialized constructions:

  • High-Layer-Count PCBs: Custom multilayer stackups with specified dielectric thickness, copper weights, and finished board thickness.
  • High-Speed PCBs: Controlled-impedance structures and low-loss laminate options.
  • RF and High-Frequency PCBs: Rogers, Isola, Taconic, PTFE, and other specified materials, subject to sourcing and process compatibility.
  • HDI PCBs: Blind and buried vias, laser microvias, and high-density interconnections.
  • Backdrilled PCBs: Through-hole stub removal for applications requiring reduced signal discontinuities.

For controlled-impedance PCBs, provide the target impedance, tolerance, layer references, dielectric requirements, and approved stackup. Our engineering team can assess whether the specified construction meets manufacturing capabilities before fabrication.

What PCB Manufacturing and Assembly Services Does EBest Circuit Offer?

EBest Circuit provides bare multilayer PCB fabrication and turnkey PCBA services, covering prototypes, small batches, and volume production.

multilayer PCB manufacturing for telecom systems, https://www.bestpcbs.com/blog/2026/10/multilayer-pcb-manufacturing-for-telecom-systems/

Our services include:

  • Custom Multilayer PCB Fabrication: FR-4, HDI, high-speed, high-frequency, and special-stackup PCB manufacturing.
  • PCB Prototyping: Engineering samples for electrical verification, mechanical evaluation, and assembly trials.
  • DFM Review: Manufacturing checks for stackups, drill structures, clearances, material compatibility, and tolerances.
  • Component Sourcing: BOM review, procurement, component availability checks, and approved alternative sourcing.
  • PCB Assembly: SMT, BGA, through-hole, and mixed-technology assembly.
  • Inspection and Testing: Bare-board electrical testing, AOI, applicable X-ray inspection, and customer-defined functional testing.
  • Volume Production: Repeat manufacturing using approved specifications, controlled revisions, and inspection requirements.

For telecom assemblies containing fine-pitch BGAs, RF connectors, shielding components, or press-fit connectors, PCB fabrication and assembly requirements are reviewed together. This helps identify potential conflicts involving board thickness, finished holes, solderability, and component placement before production.

We provide DFM guidance and manufacturing reviews based on customer-supplied designs, rather than original circuit or PCB layout design services.

What Quality Certifications and Inspection Reports Can EBest Circuit Provide?

EBest Circuit maintains quality management certifications including ISO 9001:2015, ISO 13485:2016, IATF 16949, and AS9100D. Applicable UL recognition and RoHS/REACH compliance documentation are also available according to product and project requirements.

multilayer PCB manufacturing for telecom systems, https://www.bestpcbs.com/blog/2026/10/multilayer-pcb-manufacturing-for-telecom-systems/

Customers can request relevant certification documents and inspection records during supplier qualification.

For multilayer telecom PCBs, quality inspection can include:

  • Inner-Layer AOI: Detects conductor defects before multilayer lamination.
  • Electrical Testing: Verifies continuity and isolation in finished bare PCBs.
  • Microsection Inspection: Evaluates plated-hole construction, copper thickness, and internal layer structures.
  • Impedance Testing: Verifies controlled-impedance structures against agreed test requirements.
  • PCBA Inspection: Uses AOI and X-ray inspection where appropriate for solder joints and concealed connections.
  • Functional Testing: Follows customer-defined procedures and acceptance criteria.

Electrical testing alone does not verify RF performance. If your telecom PCB requires insertion-loss, return-loss, or other RF measurements, the testing scope and acceptance limits must be agreed upon before manufacturing.

EBest Circuit also supports up to 15 years of production traceability, including relevant material, production, and inspection records according to the agreed documentation requirements.

How Long Does Multilayer Telecom PCB Manufacturing Take?

Standard FR-4 multilayer PCB prototypes can qualify for expedited manufacturing, while complex HDI, high-frequency, and hybrid-material constructions require project-specific scheduling.

PCB Layer Count Standard Lead Time Fastest Service
4 Layers 10 days 48 hours
6 Layers 10 days 72 hours
8 Layers 12 days 72 hours
10 Layers and Above Confirm per project Confirm per project

The expedited schedules apply to qualifying standard FR-4 prototypes with 0.4–1.6 mm board thickness, 0.5 oz or 1 oz copper, lead-free HASL, line width/spacing above 8 mil, and finished holes above 0.3 mm, subject to the applicable layer-count and board-size limits.

Special materials, blind and buried vias, sequential lamination, and additional testing can extend manufacturing lead time.

For PCBA orders, component availability, assembly complexity, and functional testing must also be included in production scheduling. International shipping time is quoted separately.

If you have a fixed delivery deadline, send your PCB specifications, order quantity, and required shipment date. Our team will confirm the available production schedule before order acceptance.

What Affects the Cost of Multilayer Telecom PCB Manufacturing?

Layer count, laminate selection, via structures, copper thickness, and manufacturing tolerances directly affect multilayer telecom PCB production cost. Even boards with the same dimensions and layer count can require different materials and manufacturing processes.

Cost Factor Manufacturing Impact
Layer Count and Stackup Additional materials, layer registration, and lamination requirements
Low-Loss Materials Specialized laminate sourcing, processing, and compatibility requirements
HDI and Via Structures Laser drilling, blind/buried vias, sequential lamination, and backdrilling
Copper Thickness Changes to etching limits, conductor geometry, and resin filling
Manufacturing Tolerances Tighter control of fine lines, critical dimensions, and impedance structures
Order Quantity Prototype setup, material utilization, and production planning
Assembly and Testing Component sourcing, SMT complexity, inspection, and functional verification

An 8-layer FR-4 telecom control board and an 8-layer hybrid RF PCB may have substantially different manufacturing costs because of their material, signal, and processing requirements.

When an approved design allows alternative materials or manufacturing constructions, our engineering team can assess their feasibility. Any change affecting electrical performance or approved specifications requires customer authorization.

Why Choose EBest Circuit for Multilayer Telecom PCB Manufacturing?

EBest Circuit helps telecom equipment manufacturers reduce production risks, simplify supplier coordination, and maintain consistent PCB quality across orders. With manufacturing experience dating back to 2006, we provide practical engineering and production support for complex multilayer PCB projects.

  • Fewer Manufacturing Issues: Our DFM review identifies potential problems with stackups, materials, drill structures, and board thickness before fabrication, helping you avoid unnecessary revisions and production delays.
  • Faster Technical Communication: Every EBest PCBA project is supported by a 1+3 technical team (PE + DFM + Process + Quality), giving you coordinated support for engineering questions, manufacturing requirements, and quality concerns.
  • Simplified Purchasing and Production: PCB fabrication, component sourcing, assembly, and testing can be handled through one supplier, reducing communication gaps and the time spent coordinating multiple manufacturers.
  • More Consistent Repeat Orders: Approved manufacturing files, revision control, and production traceability help maintain the required specifications across production batches and reduce the risk of unauthorized changes.
  • Experienced Manufacturing Support: With 20+ years of PCB manufacturing experience, EBest Circuit helps you evaluate complex multilayer specifications, identify practical manufacturing options, and prepare projects for production.

Case Study: Multilayer PCB Manufacturing for 5G Telecom Equipment

Project Background

A telecom equipment customer required a high-frequency multilayer PCB for a 5G tower application. The board integrated RF, antenna, digital control, and power circuits, with both PCB fabrication and assembly requirements.

Requirements and Challenges

The customer required:

  • Controlled impedance with a ±5% target tolerance.
  • Low insertion loss and stable RF signal transmission.
  • A complex multilayer stackup using suitable low-loss materials.
  • Thermal management and shielding.
  • Dense SMT and through-hole component assembly.
  • Coordinated fabrication, assembly, and performance verification.

The challenge was to preserve the specified electrical and mechanical characteristics through PCB manufacturing and assembly.

EBest Circuit’s Manufacturing Solution

EBest Circuit reviewed the fabrication files, stackup, laminate requirements, and assembly specifications before prototype manufacturing.

multilayer PCB manufacturing for telecom systems, https://www.bestpcbs.com/blog/2026/10/multilayer-pcb-manufacturing-for-telecom-systems/

The project included:

  • Material Review: Evaluating low-loss laminate requirements for the RF circuitry.
  • Prototype Validation: Checking the PCB against electrical, thermal, and assembly requirements.
  • PCB Fabrication and Assembly: Coordinating multilayer fabrication, SMT assembly, and through-hole assembly.
  • Quality Inspection: Performing agreed inspection and verification procedures.

Project Results

The prototype met the customer’s RF, thermal, and assembly requirements and progressed into batch production. Manufacturing and assembly requirements were carried forward into production, supporting consistent quality and on-time delivery.

What Information Is Needed for a Multilayer Telecom PCB Quote?

You can request an initial manufacturing assessment with your basic PCB specifications and expected quantity. Complete fabrication files are useful for detailed engineering review but are not required for the first inquiry.

For an initial quotation, provide:

  • PCB Specifications: Layer count, dimensions, finished thickness, copper weights, and preferred materials.
  • Special Requirements: Controlled impedance, HDI structures, backdrilling, special finishes, or additional inspection.
  • Order Details: Prototype quantity, expected production volume, delivery location, and required shipment date.
  • Service Scope: Bare PCB fabrication or PCB manufacturing with component sourcing and assembly.

For detailed manufacturing approval, provide Gerber or ODB++ files, drill data, fabrication drawings, and stackup specifications. PCBA orders also require the relevant BOM, placement data, assembly drawings, and testing instructions.

Send your requirements to sales@bestpcbs.com. Our engineering team will review manufacturing feasibility, clarify technical specifications, and prepare a quotation based on your project.

Frequently Asked Questions About Multilayer Telecom PCBs

Q1: Can I specify IPC Class 3 acceptance for telecom PCBs?

A1: Yes. IPC Class 3 acceptance can be specified when required by the product. Confirm the applicable standard, revision, inspection criteria, and documentation before production.

Q2: Can different dielectric materials be combined in one multilayer PCB?

A2: Yes. Hybrid stackups can combine compatible materials, provided their electrical properties, thermal behavior, and lamination requirements are suitable.

Q3: Can I supply my own RF components for PCB assembly?

A3: Yes. Customer-supplied components can be used after confirming package compatibility, handling requirements, quantities, and incoming inspection conditions.

Q4: Are impedance test coupons required for every telecom PCB?

A4: No. They are used when controlled-impedance verification is specified. Coupon construction, target values, and acceptance criteria should be defined before fabrication.

Q5: Can EBest Circuit combine high-density BGA routing and high-current circuits on one PCB?

A5: Yes, subject to manufacturing review. Copper distribution, routing density, via structures, thermal requirements, and assembly constraints must be compatible.

Q6: Can the laminate brand be changed between production batches?

A6: Not without customer approval when the material is specified or controlled. Any proposed alternative must be evaluated for electrical, thermal, mechanical, and manufacturing compatibility.

Q7: What happens if the Gerber files conflict with the fabrication drawing?

A7: The conflicting requirements must be resolved before production. Fabrication proceeds using the confirmed file revision and approved manufacturing instructions.

Q8: Can EBest Circuit provide production lot identification for repeat orders?

A8: Yes. Production lot identification and related manufacturing records can be arranged according to the project’s traceability requirements.

Q9: Are customer-provided test fixtures or firmware needed for functional testing?

A9: They may be required. Functional testing often depends on customer-defined procedures, fixtures, firmware, and pass/fail criteria that should be confirmed before assembly.

Conclusion: Get a Quote for Your Multilayer Telecom PCB Project

Reliable multilayer PCB manufacturing for telecom systems depends on compatible materials, manufacturable stackups, controlled dimensions, and clearly defined electrical requirements. Confirming these specifications before fabrication helps prevent unnecessary production changes and quality issues.

EBest Circuit provides multilayer PCB fabrication, DFM review, prototyping, component sourcing, PCBA assembly, and inspection services for telecom OEMs and equipment manufacturers. Send your PCB specifications, quantities, and delivery requirements to sales@bestpcbs.com for a manufacturing feasibility review and quotation.

You may also like

IoT Controller and Switch PCB Assembly Service, Turnkey Solutions

October 22nd, 2026

IoT controller and switch PCB assembly requires reliable switching circuits, wireless communication, and stable power management. These assemblies are widely used in smart switches, relay controllers, lighting systems, and industrial control equipment. Manufacturing quality depends on component accuracy, SMT/THT soldering, electrical isolation, and functional testing.

EBest Circuit provides turnkey IoT controller and switch PCB assembly services, covering PCB fabrication, component sourcing, SMT/THT assembly, inspection, and testing support. From prototypes to volume production, we help OEM customers reduce manufacturing risks, simplify supplier coordination, and maintain consistent assembly quality.

IoT Controller and Switch PCB Assembly, https://www.bestpcbs.com/blog/2026/10/iot-controller-and-switch-pcb-assembly/

What Does Turnkey IoT Controller and Switch PCB Assembly Include?

Turnkey IoT controller and switch PCB assembly combines PCB manufacturing, component procurement, assembly, and agreed testing within one coordinated production service. Instead of managing separate PCB and component suppliers, customers can work with one manufacturing partner using their approved production files.

EBest Circuit supports different sourcing arrangements:

Service Option Scope of Service Suitable For
Full Turnkey PCBA PCB fabrication, approved component sourcing, SMT/THT assembly, inspection, and agreed testing OEM customers seeking one manufacturing partner
Partial Turnkey PCBA EBest sources selected components while customers supply designated parts Projects using customer-controlled MCUs, relays, or wireless modules
Consigned PCB Assembly Customers supply the required components, with PCB fabrication and assembly arranged according to the order Projects with established component supply channels

Firmware programming, custom test fixtures, and additional product integration can be included when agreed during project review.

Turnkey manufacturing begins with customer-approved PCB and assembly data. EBest provides DFM guidance and manufacturing review rather than original circuit design.

What Types of IoT Controllers and Smart Switches Need Custom PCB Assembly?

Custom IoT controller and switch PCB assemblies are used in connected devices that receive commands and control electrical loads. Different applications require different switching components, communication interfaces, and assembly processes.

  • Smart Wall Switches: Combine wireless modules, switching devices, and power circuits in compact enclosures. Reliable terminal connections and appropriate electrical separation are essential.
  • Multi-Channel Relay Controllers: Control multiple electrical outputs independently. Relay positioning, through-hole soldering, and output channel identification require careful inspection.
  • Smart Lighting Controllers: Use MOSFETs, relays, or dimming circuits to regulate lighting loads. Power component soldering and thermal management affect operating reliability.
  • Industrial Remote Switching Boards: Connect control signals to actuators, relays, and other equipment. Connector stability, electrical protection, and operation in industrial environments are major considerations.
  • HVAC and Motor Control Modules: Switch fans, pumps, and other inductive loads. These assemblies require suitable power connections, switching components, and application-specific verification.

The load type determines many of the manufacturing and testing requirements. A low-voltage lighting controller and a mains-powered relay switch may use similar wireless modules, but their current-carrying, electrical isolation, and switching requirements are different.

What Are the Key Assembly Requirements for IoT Controllers and Smart Switches?

Reliable IoT controller and switch PCB assembly depends on accurate component installation, suitable soldering processes, and consistent assembly quality. Switching devices and power connections require particular attention because poor solder joints can cause intermittent operation or overheating.

Component or Assembly Area Assembly Requirements Potential Problems
Relays and Terminal Blocks Correct orientation, suitable through-hole soldering, and secure connections Weak solder joints, insufficient hole fill, or incorrect installation
MOSFETs and Power Devices Adequate solder coverage, thermal pad attachment, and alignment Poor thermal contact, solder defects, or overheating
Wireless Modules Approved reflow conditions, moisture-sensitive handling, and accurate placement Solder damage, assembly defects, or reduced wireless performance
MCU and Driver ICs Accurate solder paste printing, polarity control, and placement Solder bridges, open connections, or incorrect orientation
Electrical Isolation Areas Preserve specified separation features and prevent solder bridges or contamination Reduced insulation performance or electrical safety risks

Mixed SMT/THT assembly is common in IoT relay controllers. Small ICs, resistors, and wireless modules are typically assembled using SMT, while relays and larger terminal blocks may require through-hole soldering.

These components cannot always use the same soldering process. Relay housings and plastic connectors may have different temperature limits, while power components require suitable solder joint formation to maintain reliable electrical and thermal connections.

What Should You Check Before IoT Controller and Switch PCB Manufacturing?

Before releasing production files, confirm the PCB specifications, component footprints, electrical isolation features, and assembly constraints. Early DFM review helps identify manufacturing conflicts before materials are purchased or boards are fabricated.

  • PCB Fabrication Requirements: Check the layer stackup, board thickness, copper weight, hole dimensions, surface finish, and specified manufacturing tolerances.
  • Electrical Isolation Features: Verify that the manufacturing data preserves the approved creepage distances, clearances, slots, and separation between high- and low-voltage sections.
  • Relay and Connector Footprints: Confirm pin arrangements, drill sizes, pad dimensions, and mechanical positioning against the approved component specifications.
  • Power and Thermal Features: Review the manufacturability of specified copper thickness, thermal vias, exposed pads, and heat-dissipation structures.
  • Wireless Module Requirements: Verify that the approved antenna keepout areas and assembly restrictions are maintained.
  • Panelization and Mechanical Constraints: Check board outlines, mounting holes, component-to-edge distances, and depaneling methods to reduce mechanical stress on mounted components.

DFM review identifies manufacturing risks but does not replace electrical design validation. Any proposed changes affecting circuitry, component selection, or electrical isolation must be approved by the customer’s engineering team.

How Are IoT Controller and Switch PCBs Manufactured and Assembled?

Turnkey IoT controller and switch PCB manufacturing follows a controlled process from component procurement to final assembly inspection. The assembly sequence must accommodate compact wireless electronics alongside relays, connectors, and power components.

IoT Controller and Switch PCB Assembly, https://www.bestpcbs.com/blog/2026/10/iot-controller-and-switch-pcb-assembly/

Step 1: PCB Fabrication

Manufacture the bare PCB according to the approved stackup, copper specifications, drill files, and surface finish. Inspect critical dimensions and electrical separation features, then complete the specified bare-board electrical testing.

Step 2: Component Sourcing and Verification

Procure the approved MCUs, wireless modules, relays, MOSFETs, connectors, and passive components. Verify part numbers, packaging conditions, and component handling requirements. Substitutions require customer approval.

Step 3: SMT Assembly

Apply solder paste, place SMD components, and complete reflow soldering using a qualified process. Fine-pitch controller ICs, wireless modules, and power devices require careful placement and solder joint control.

Step 4: Through-Hole Assembly

Install relays, terminal blocks, and other THT components using an appropriate soldering method, such as selective soldering, wave soldering, or controlled manual soldering.

Through-hole solder fill, terminal alignment, and component temperature limits are particularly important for relay-based switching boards.

Step 5: Assembly Inspection

Use visual inspection and AOI to identify applicable placement and soldering defects. X-ray inspection may be used for components with hidden solder joints.

Inspect relay pins, terminal connections, and other areas not fully covered by AOI using suitable inspection methods.

Step 6: Programming, Testing, and Packaging

Perform the agreed firmware programming and functional tests using customer-provided instructions and acceptance criteria. Package finished PCB assemblies with appropriate ESD and mechanical protection, along with specified identification labels.

How Are IoT Controller and Switch PCB Assemblies Tested?

Functional testing verifies whether an assembled controller powers up, processes commands, and operates its switching outputs correctly. Inspection alone cannot confirm that a relay controller or smart switch will operate as intended.

IoT Controller and Switch PCB Assembly, https://www.bestpcbs.com/blog/2026/10/iot-controller-and-switch-pcb-assembly/
Test Item What Is Checked Possible Failure Indication
Power-Up Test Supply voltage, regulated outputs, startup behavior, and current consumption No startup, abnormal current, or unexpected reset
MCU and Firmware Test Firmware version, control inputs, and output commands Incorrect firmware, missing response, or wrong output mapping
Relay Switching Test Relay activation, NO/NC contact operation, and channel switching Relay fails to operate or switches the wrong channel
MOSFET Output Test Switching waveform, output voltage, and specified current behavior Missing output, incorrect switching, or abnormal voltage drop
Wireless Communication Test Module initialization, connection, command reception, and response Failed connection, missing response, or unstable communication
Load and Thermal Validation Switching operation and temperature under specified operating loads Unexpected reset, excessive heating, or unstable switching

Production functional testing and product qualification testing should be defined separately. Routine production tests may cover power, firmware, communication, and switching outputs, while extended load cycling, thermal testing, and electrical safety verification may require dedicated qualification procedures.

For example, a relay controller may operate normally without a load but reset when switching an inductive device. Representative load testing can identify problems that basic continuity checks cannot reveal.

EBest Circuit supports customer-defined functional testing, with the testing scope, equipment, and acceptance criteria confirmed before production. Product-level safety and wireless certification remain separate from routine PCBA inspection.

How Can You Validate Prototypes Before Mass Production?

Prototype validation should establish an approved manufacturing configuration that can be reproduced in later production batches. Passing a functional test on one sample does not automatically confirm that the assembly process is ready for volume production.

Step 1: Review Prototype Manufacturing Results

Check the initial assemblies for solder defects, component discrepancies, manufacturing deviations, and mechanical fit issues. Resolve identified problems before production approval.

Step 2: Approve the Production Configuration

Confirm the PCB revision, BOM, approved component substitutions, assembly drawings, and firmware version. Different product variants should use clearly identified configurations.

Step 3: Establish Repeatable Production Controls

Approve assembly instructions, inspection requirements, programming procedures, and functional test criteria. Record the accepted process requirements for future orders.

Step 4: Verify the Initial Production Batch

Perform first-article inspection and verify that production units match the approved configuration. Record deviations and obtain the necessary approvals before releasing affected assemblies.

Controlled BOM revisions, firmware identification, and production records help prevent mixed configurations and inconsistent assembly quality. These controls are especially useful when one IoT controller platform supports several switching variants.

What Affects IoT Controller and Switch PCB Assembly Lead Time?

Component availability, PCB fabrication requirements, mixed SMT/THT assembly, and test preparation are the main factors affecting turnkey IoT controller and switch PCB assembly lead time.

Lead Time Factor Impact on Production
Relay and Wireless Module Availability Long-lead components or unavailable approved part numbers can delay material preparation
PCB Fabrication Requirements Special copper thickness, manufacturing tolerances, or additional processes may extend fabrication
Mixed SMT/THT Assembly Relays, connectors, and other through-hole components require additional assembly operations
Firmware and Test Preparation Incomplete programming instructions or unavailable test fixtures can delay production release
Engineering Changes Revised PCB files, BOM changes, or substitutions may require additional review and approval

Finalizing the BOM, PCB revision, assembly instructions, and testing requirements before order release helps reduce avoidable delays.

For repeat production, notify the manufacturer of component, firmware, or hardware changes before procurement begins. Even when the PCB layout remains unchanged, these changes may affect assembly preparation and testing.

Why Choose EBest Circuit for Turnkey IoT Controller and Switch PCB Assembly?

EBest Circuit provides integrated PCB manufacturing, component sourcing, SMT/THT assembly, and testing support for custom IoT controllers and smart switches. Our turnkey services help OEM customers coordinate manufacturing activities while maintaining approved component and quality requirements.

  • One-Stop PCB and PCBA Manufacturing: Coordinate PCB fabrication, component sourcing, mixed SMT/THT assembly, inspection, and agreed testing through one manufacturing partner rather than multiple separate suppliers.
  • 1+3 Technical Team: Every EBest PCBA project is supported by a 1+3 technical team (PE + DFM + Process + Quality) to review manufacturability, component requirements, assembly processes, and quality risks before production.
  • Component Sourcing and BOM Control: Verify approved component specifications and manage substitutions with customer authorization, helping prevent incorrect relays, wireless modules, or other components from entering production.
  • Inspection and Functional Testing Support: Combine assembly inspection with customer-defined electrical and functional testing to identify applicable soldering, component, and switching faults before delivery.
  • Prototype-to-Production Support: Maintain approved PCB revisions, assembly instructions, component records, and inspection requirements as projects move from sample builds to repeat orders.
  • Quality Management and Traceability: EBest Circuit holds ISO 9001, ISO 13485, IATF 16949, and AS9100D certifications and supports production traceability records for up to 15 years, subject to applicable project requirements.

For OEM customers, turnkey manufacturing reduces the number of suppliers that must be coordinated, while controlled component sourcing, assembly procedures, and inspection records help maintain consistency across production batches.

What Information Do You Need for a Turnkey IoT Controller and Switch PCBA Quote?

A complete RFQ package helps confirm the turnkey manufacturing scope, component availability, assembly requirements, and testing arrangements.

Please provide:

  • PCB Manufacturing Files: Gerber or ODB++ data, drill files, stackup, board thickness, copper specifications, and fabrication drawings.
  • Assembly Files: Approved BOM, manufacturer part numbers, CPL/pick-and-place files, and assembly drawings.
  • Electrical Requirements: Input voltage, output ratings, load type, switching configuration, and applicable insulation requirements.
  • Programming and Testing: Firmware files where required, programming instructions, test procedures, and acceptance criteria.
  • Order Information: Prototype or production quantity, hardware revision, required delivery schedule, and shipping destination.
  • Turnkey Scope: Confirm whether you need full turnkey manufacturing, partial component sourcing, or assembly using customer-supplied parts.

Send your production files to sales@bestpcbs.com for manufacturing review and a project-specific quotation.

FAQs About IoT Controller and Switch PCB Assembly

Q1: Who owns custom test fixtures after a turnkey PCBA order is completed?

A1: Ownership depends on the agreed purchase and tooling terms. Customer-funded fixtures can be returned, retained for repeat orders, or handled under another agreed arrangement. Confirm ownership and storage requirements before production.

Q2: Can relay PCB assemblies be cleaned after soldering?

A2: It depends on the relay construction and manufacturer instructions. Not all relays are suitable for PCB washing. Cleaning fluids or moisture entering an unsealed relay can affect contact performance.

Q3: Does conformal coating affect smart switch components?

A3: It can. Relay vents, connector contacts, mechanical switches, and other sensitive areas may require masking. Coating compatibility and exclusion areas should be confirmed before application.

Q4: How should ESD-sensitive wireless modules be handled?

A4: Wireless modules and controller ICs should be handled using appropriate ESD-protected packaging, workstations, and storage procedures. Moisture-sensitive devices must also follow their specified handling and reflow requirements.

Q5: Can lead-free soldering be used for smart switch PCB assemblies?

A5: Yes, provided the PCB materials and components are compatible with the selected process. The solder alloy, soldering method, and temperature profile must remain within the applicable component limits.

Q6: Can assembled controller PCBs include serial numbers or QR codes?

A6: Yes. Customer-defined serial numbers, QR codes, or labels can identify individual assemblies, hardware revisions, and production batches. The marking method and required traceability information should be agreed before production.

Q7: How should assembled relay controller PCBs be packaged for shipping?

A7: Finished boards should use suitable ESD-protective packaging and mechanical protection for protruding relays, terminals, and connector pins. Packaging should prevent electrostatic damage, component movement, and mechanical stress during transportation.

Q8: Is burn-in testing necessary for every IoT smart switch PCB?

A8: Not necessarily. Burn-in requirements depend on the product’s reliability targets and qualification plan. Routine functional testing does not automatically require extended burn-in, and additional screening should use agreed test conditions and acceptance criteria.

Conclusion

Reliable IoT controller and switch PCB assembly requires accurate component sourcing, controlled SMT/THT processes, and functional testing matched to the intended switching application. A coordinated turnkey manufacturing process helps reduce supplier handoffs while maintaining consistent assembly requirements from prototypes to volume production.

EBest Circuit provides turnkey IoT controller and switch PCB assembly solutions for OEM customers worldwide. From PCB fabrication and component procurement to assembly, inspection, and testing support, we help bring your approved controller design into production. Send your Gerber files, BOM, assembly requirements, and order quantity to sales@bestpcbs.com for DFM review and a customized manufacturing quotation.

You may also like

Custom Traction Inverter PCB Manufacturer in China

October 22nd, 2026

A custom traction inverter PCB needs reliable fabrication, an assembly process suited to its components and engineering support that keeps production aligned with the design. EBest Circuit provides custom PCB manufacturing and assembly for control, sensing and gate-driver interface boards used in traction inverter development.

With high-Tg multilayer fabrication, component sourcing, SMT and THT assembly, and inspection support, EBest Circuit helps you coordinate the transition from PCB files to assembled boards. Send your design files and quantity to sales@bestpcbs.com for a manufacturing review and quotation.

traction inverter PCB
AI-generated application illustration of a traction inverter control PCB and inverter assembly.

Traction Inverter PCB Types Manufactured by EBest Circuit

EBest Circuit manufactures boards to your design, matching the materials, copper construction and assembly process to each board’s function.

  • Control PCBs — Multilayer construction supports processors, communication interfaces and mixed-signal circuitry. Stackup review helps accommodate dense routing, reference planes and the required finished thickness.
  • Gate-Driver and Driver-Interface PCBs — Fabrication preserves specified isolation boundaries, compact driver connections and local supply routing. Copper geometry, solder-mask openings and component clearances receive particular attention.
  • Sensing and Feedback PCBs — Boards for current, voltage and temperature feedback benefit from accurate conductor patterns, controlled assembly and cleanliness around sensitive measurement circuits.
  • Auxiliary Power and Interface PCBs — Copper weight, plated holes and connector mounting are matched to local power distribution and interconnection requirements.

Each board is specified for its own electrical and mechanical duties. This keeps fabrication choices relevant to the application instead of applying the same construction across the entire inverter.

Custom Traction Inverter PCB Manufacturing Capabilities

EBest Circuit offers multilayer FR-4 fabrication with high-Tg materials, heavier copper, controlled impedance and blind or buried via options. The following parameters provide a starting point for evaluating your design.

Manufacturing Parameter Standard Process Range Special Process Options
FR-4 Layer Count 1–10 layers 10–32 layers, subject to construction review
Inner-Layer Copper 0.5–5 oz 5–20 oz
Outer-Layer Copper 1–5 oz 5–20 oz
High-Tg FR-4 Tg 170–180°C material options Additional grades subject to material and process review
Board Thickness for ENIG 0.4–3.5 mm Thinner or thicker constructions evaluated individually
Minimum Finished Hole Diameter 0.20 mm 0.15 mm
Maximum Through-Hole Aspect Ratio 8:1 10:1
Inner-Layer Trace/Spacing at 2 oz Copper 6/6 mil 5/5 mil
Outer-Layer Trace/Spacing at 2 oz Copper 8/8 mil 6/6 mil
Surface Finish Options ENIG, OSP, HASL, immersion silver, immersion tin and ENEPIG Selected according to assembly and contact requirements

Capability limits depend on the complete board construction. Copper weight, spacing, hole size and board thickness are reviewed together; their individual limits are not automatically available in the same design. Early review helps retain critical features without adding unnecessary process complexity.

PCB Materials and Stackup Options for Traction Inverters

EBest Circuit reviews material and stackup choices against your board’s thermal, insulation, routing and assembly requirements. Available high-Tg FR-4 options include grades such as S1000-2 and IT180, with the specific laminate agreed before production.

Material or Construction Option Suitable Application Manufacturing Focus
High-Tg FR-4 Control and interface boards requiring a specified laminate for assembly and thermal conditions Material grade, finished thickness and compatibility with the assembly process
Higher-CTI Material Options Boards with insulation barriers where tracking resistance influences the design Material CTI, creepage requirements and availability of the specified grade
Four-Layer Stackup Control, sensing and driver-interface boards with moderate routing density Signal routing, reference-plane arrangement and copper balance
Higher-Layer-Count Stackup Dense processors, multiple interfaces and complex power distribution Layer registration, dielectric construction and via structure
Heavier-Copper Construction Local supply distribution and conductors requiring greater cross-section Copper-dependent spacing, etching allowances and soldering behavior

Material selection and stackup planning work together. Tg alone does not establish continuous operating temperature or insulation capability. Where controlled impedance is required, EBest Circuit can review production dielectric thicknesses and conductor geometry before fabrication.

DFM and Layout Support for Traction Inverter PCBs

EBest Circuit’s DFM support focuses on resolving manufacturing issues before they become production delays. Engineering questions connect the supplied layout with the proposed fabrication and assembly processes.

  • Copper Geometry Review — Checks trace widths and spacing against the selected copper weight, helping avoid features that become difficult to reproduce after etching.
  • Drill and Via Review — Evaluates finished hole sizes, annular rings and thickness-to-hole relationships to identify plating and interconnection concerns.
  • Isolation Features and Slots — Reviews the manufacturability of specified gaps, routed slots and copper keepouts while preserving the design’s electrical boundaries.
  • Solder-Mask and Pad Review — Checks openings, mask bridges and via treatment around component pads to support consistent solder-paste deposition and assembly.
  • Stackup and Panel Review — Coordinates finished thickness, layer construction, tooling features and panel support with fabrication and component placement.

Changes affecting electrical behavior are returned for design approval. This gives your engineering team visibility into proposed adjustments while allowing manufacturing questions to be resolved before production release.

Traction Inverter PCB Assembly Services

EBest Circuit combines PCB fabrication and assembly support so board construction, components and inspection requirements can be managed within one project.

  • Component Sourcing — Procurement follows the agreed BOM, with component questions and proposed substitutions raised for approval. This helps align purchasing with the intended circuit and package requirements.
  • SMT Assembly — Supports surface-mount control, sensing and driver-interface circuitry. Stencil preparation and reflow planning account for component size, pad design and copper distribution.
  • THT Assembly — Supports through-hole connectors and other leaded components, with attention to hole fit, solder access and mechanical mounting requirements.
  • Mixed-Technology Assembly — Coordinates SMT and THT operations for boards combining compact electronics with larger connectors or supporting components.
  • AOI and X-Ray Inspection — Provides inspection of visible assembly features and, where appropriate, hidden solder joints according to the agreed inspection plan.
  • Functional Testing Support — Testing can be scoped around customer-defined fixtures, firmware, interfaces and acceptance limits to assess the required board functions.

Coordinating these services helps resolve fabrication and assembly interactions early, including panel handling, connector access and the soldering demands of heavier copper.

Quality Control and Testing for Traction Inverter PCBs

EBest Circuit aligns inspection with the board construction and assembly requirements. Each method addresses a specific manufacturing concern.

  • PCB Dimensional and Construction Checks — Verify relevant features such as finished thickness, conductor geometry, plated-hole copper and surface finish against the manufacturing specification.
  • Bare-Board Electrical Testing — Checks circuit connectivity to identify opens and shorts before components are installed.
  • Automated Optical Inspection — Examines visible component placement, polarity and solder-joint features to help detect assembly defects.
  • X-Ray Inspection — Supports evaluation of hidden solder connections where package construction limits optical access.
  • Cleanliness Inspection — Checks for solder balls, debris and unwanted residues, particularly around sensitive circuits and isolation regions.
  • Agreed Functional Tests — Evaluate specified circuit functions using defined conditions and acceptance criteria.

Manufacturing inspection and application qualification serve different purposes. Insulation, environmental and system-level validation requirements should be defined for the intended application so the production and test scope can support them.

Custom Traction Inverter PCB Manufacturing Case Study

Application: A representative traction inverter control and gate-driver interface board combines PWM interfaces, sensing connections and local supply distribution near the power stage. The following application example uses an actual EBest Circuit four-layer PCB specification, with the construction matched to this engineering scenario.

Manufacturing Challenges:

  • Heavier copper alongside compact circuitry. The 2 oz copper construction requires suitable etching allowances to preserve conductor widths and spacing around smaller components.
  • Consistent plated-hole construction. The specified minimum hole-wall copper thickness of 25 μm requires attention to drilling, plating and verification.
  • Different soldering demands across the board. Larger copper areas draw heat away from pads differently than smaller signal features, affecting solder-paste and reflow preparation.

EBest Circuit’s Solutions: The selected construction uses S1000-2M FR-4 with Tg170, four copper layers and a finished thickness of 1.6 mm ±10%. For this application, DFM review would check fine features against the 2 oz process and coordinate the stackup and panel before fabrication. Drill and plating planning would address the hole-wall copper requirement, followed by bare-board electrical testing.

ENIG provides a flat surface for component attachment. Assembly preparation would account for the copper distribution and component thermal mass, with AOI, X-ray and cleanliness checks included in the corresponding assembly requirements.

Customer Benefits: This approach connects copper geometry, plated-hole quality and soldering behavior in one manufacturing plan. It helps reduce avoidable fabrication and assembly rework while providing an inspectable board platform for inverter integration and testing. The four-layer construction also offers routing flexibility without introducing a more complex HDI structure solely for this representative application.

PCB Specifications:

PCB Parameter Selected Specification
PCB Type Rigid multilayer FR-4 PCB
Application Traction inverter control and gate-driver interface board — representative application
Layer Count 4 layers
Base Material S1000-2M FR-4, Tg170
Board Thickness 1.6 mm ±10%
Finished Copper Thickness 2 oz on inner and outer layers
Surface Finish ENIG; gold 1 μin, nickel 100 μin
Minimum Hole-Wall Copper Thickness 25 μm
Solder Mask / Legend Blue solder mask / white legend
Inspection Requirements Bare-board electrical testing; AOI and X-ray for the corresponding assembly
traction inverter PCB
Representative control and driver-interface PCB illustration; not a photograph of the case-study board.

400 V vs. 800 V Traction Inverter PCB Requirements

The voltage across each circuit and isolation barrier determines the relevant PCB requirements. Moving to an 800 V platform does not automatically mean doubling every clearance or increasing copper thickness throughout the board.

Design Consideration 400 V Traction Inverter Platform 800 V Traction Inverter Platform
Voltage Specification Establish maximum operating voltage and transients for each circuit Reassess circuit and barrier stresses for the higher-voltage platform
Creepage and Clearance Derived from insulation requirements, material and environment Often more demanding where the higher voltage appears across a barrier
Material Evaluation Assess thermal properties, CTI and dielectric construction Recheck these properties against the revised insulation requirements
Gate-Driver Layout Depends on switching devices, edge rates and driver architecture Fast-switching designs can place greater demands on parasitic coupling and return-path control
Voltage Sensing Divider ratings, spacing and measurement range match the monitored voltage Divider construction and component voltage distribution may require revision
Copper Thickness Determined by local current and allowable temperature rise Still determined by local current and temperature rise; voltage alone does not require thicker copper
Validation Test against defined circuit and insulation requirements Update test conditions and acceptance limits for the revised design

EBest Circuit can review the fabrication implications of revised spacing, slots, stackups and component layouts. The focus is on identifying necessary manufacturing changes while retaining suitable features from the existing design.

traction inverter PCB
Conceptual comparison of 400 V and 800 V platforms; requirements depend on circuit voltage and design.

Why Choose EBest Circuit as Your Traction Inverter PCB Manufacturer?

EBest Circuit brings together fabrication options, engineering review and assembly support to help customers move from a defined design to a manufacturable board.

  • Custom Construction Matched to Your Design — Layer count, copper weight, material and surface finish can be selected around the board’s function, helping avoid unnecessary process cost.
  • DFM Support Before Production — Review of copper features, holes, solder mask and panels identifies issues while adjustments are still manageable.
  • Coordinated PCB Fabrication and Assembly — Related decisions, including finish selection, panel support and soldering requirements, can be addressed within one project workflow.
  • Component Procurement Alongside Assembly — BOM review and sourcing support connect purchasing decisions with package, placement and circuit requirements.
  • Inspection Suited to the Board — Electrical testing, AOI, X-ray and agreed functional checks provide distinct checks for fabrication and assembly quality.
  • Engineering Communication Around Changes — Production questions and proposed adjustments are raised for approval, helping preserve design intent and clarify what will be manufactured.

For engineers, these services provide practical support for resolving production details. For procurement teams, they help establish a clearer quotation, manufacturing scope and inspection requirement.

How to Get a Quote for Traction Inverter PCBs?

Email sales@bestpcbs.com with your PCB files and required quantity to request a quotation for bare-board fabrication or PCB assembly.

Include the following items where applicable:

  • PCB Manufacturing Files — Gerber files, drill data and the fabrication drawing.
  • Construction Requirements — Stackup, material, finished thickness, copper weights and surface finish.
  • Special Features — Controlled impedance, via filling, blind or buried vias, slots and critical tolerances.
  • Assembly Files — BOM, component placement data and assembly drawings.
  • Inspection and Test Requirements — Programming, functional testing and any specified acceptance criteria.
  • Order Details — Quantity and required delivery date.

If the construction is still being finalized, send the proposed stackup and application requirements. EBest Circuit can discuss manufacturing options before the final production files are released.

FAQs About Traction Inverter PCB Manufacturing

Can an industrial inverter PCB be used directly in an automotive traction inverter?

Not automatically. A similar construction may be a starting point, but suitability depends on the vehicle program’s electrical, environmental and quality requirements. Matching material and layer count alone is insufficient.

Does Tg170 mean the assembled board can operate continuously at 170°C?

No. Tg describes the laminate’s glass-transition behavior. Continuous operating limits also depend on long-term material properties, components, solder joints and the application conditions.

Does blue solder mask provide additional high-voltage insulation?

Color does not establish an insulation rating. Any insulation credit must be supported by the specific solder-mask material, thickness, process and applicable qualification.

Can solder-mask plugging replace resin-filled and copper-capped vias?

No. These processes create different structures. Via-in-pad designs may require filling, planarization and copper capping to control solder loss and provide a suitable component mounting surface.

Will changing the surface finish affect assembly?

It can. Surface finish influences pad flatness, solderability, storage requirements and process behavior. Changes should be reviewed against the component and assembly requirements.

Does a 2 oz copper PCB have a fixed current rating?

No. Current capacity also depends on conductor dimensions, layer position, cooling and allowable temperature rise. Copper weight alone does not define the board’s current rating.

Can a replacement component be fitted without changing the PCB?

Sometimes, but footprint compatibility is only one consideration. Pin function, electrical ratings, package tolerances, isolation properties and thermal behavior must also match the application.

Ready to move your traction inverter PCB into production? Send your design files, quantity and assembly requirements to sales@bestpcbs.com for a custom EBest Circuit quotation.

You may also like

Satellite PCB Assembly Services, High Reliability & Full Traceability

October 14th, 2026

Satellite PCB assembly services turn your approved design into assembled, inspected, and tested boards for satellite electronics. High reliability depends on suitable materials, sound solder joints, cleanliness, and mechanical support. Full traceability connects delivered boards to their components, build revisions, production history, and test results.

At EBest Circuit, a dedicated engineering team coordinates PCB fabrication, component sourcing, assembly, and agreed testing. Before production, we review your files, identify manufacturing concerns, and confirm component availability and inspection requirements, helping you prepare for system integration with fewer unresolved assembly questions.

satellite PCB assembly, https://www.bestpcbs.com/blog/2026/10/satellite-pcb-assembly/

What Is Satellite PCB Assembly?

Satellite PCB assembly is the process of mounting and soldering electronic components onto a printed circuit board to create a functional assembly for satellite electronics. It establishes the electrical connections between components that allow the board to perform its intended function.

Where Are Satellite PCB Assemblies Used?

Satellite PCB assemblies support onboard computing, communications, power distribution, attitude control, and payload operation.

Application Electronic Function Assembly Priorities
Onboard computers Command processing, data handling, and storage Fine-pitch joints, memory placement, programming, and connectors
Communication modules Command reception, telemetry, and RF transmission RF components, shielding, grounding, and connector installation
Power systems Voltage conversion, protection, and distribution High-current joints, thermal paths, and load testing
Attitude-control electronics Sensor acquisition and actuator control Sensor orientation, component retention, and interface checks
Payload electronics Imaging, measurement, sensing, and processing Dense packaging, cleanliness, mechanical fit, and functional testing

A communication board may require inspection of RF connectors and shielding connections. A power board may need closer attention to large solder joints, heat distribution during assembly, and performance under specified loads.

What Are the Reliability Requirements for Satellite PCB Assembly?

Satellite PCB assembly requires dependable connections, compatible materials, secure components, and workmanship suited to the mission environment.

  • Launch vibration and shock: Connectors, larger components, and unsupported structures can transfer mechanical loads into solder joints. Design-specified staking, fastening, or supports help manage these stresses.
  • Temperature changes: Packages and PCB materials expand at different rates, placing stress on connections. Material selection, package geometry, solder joint formation, and the expected temperature range must work together.
  • Vacuum compatibility: Laminates, adhesives, coatings, labels, and process residues must satisfy the project’s material and contamination requirements.
  • Long operating periods: Stable connections, suitable handling, and consistent assembly support service-life requirements alongside design validation and qualification.

Cleanliness is especially important near contamination-sensitive equipment. Material selection, cleaning, and curing must address applicable contamination and outgassing requirements. sma.nasa.gov

Radiation requirements influence component selection and circuit design. The assembly service should preserve those decisions through approved parts, handling instructions, and substitution controls.

Specify the workmanship standard, revision, acceptance criteria, and additional space-hardware requirements before production.

How Are PCB Materials and Components Selected for Satellite PCB Assembly?

Materials and components are selected according to electrical performance, temperature exposure, mechanical demands, and project qualification requirements.

PCB materials and construction

Laminate selection considers thermal expansion, dielectric performance, moisture behavior, and compatibility with assembly temperatures. High-Tg FR-4, polyimide, and low-loss materials serve different needs; the choice should follow the board’s requirements.

Stackup and copper distribution also affect assembly. Heavy copper and large ground connections draw heat away from soldering locations, while thin boards may need support during printing, placement, or reflow.

Components and approved sources

The BOM should identify manufacturer part numbers, packages, approved alternatives, and sourcing or screening restrictions. Include required lot information and documentation for critical devices.

Moisture-sensitive components need appropriate storage and preparation. Customer-supplied parts should arrive with sufficient packaging and exposure-history information to determine their handling requirements.

Soldering and post-processing materials

Surface finishes, solder alloys, fluxes, cleaners, adhesives, and coatings must be compatible. Their combination affects wetting, residue removal, curing, inspection, and repair.

Outgassing data can assist spacecraft material evaluation, with suitability assessed against the project’s application and conditions.

Review alternatives beyond footprint compatibility. Ratings, finish, thermal behavior, firmware dependencies, and qualification history can affect whether a substitute is acceptable.

How Does DFM Review Improve Satellite PCB Assembly Reliability?

DFM review identifies manufacturing problems before they lead to defective assemblies, purchased-material losses, or production delays.

  • File inconsistencies: Conflicting BOMs, drawings, placement data, or PCB revisions can result in incorrect components or orientations.
  • Soldering difficulties: Pad dimensions, paste openings, spacing, and uneven thermal connections can contribute to bridging, insufficient solder, or component movement.
  • Handling concerns: Board thickness, edge-mounted parts, panel features, and depaneling clearance affect assembly stability and damage risk.
  • Limited inspection access: Shields, tall components, and restricted test points can obstruct important checks.

For example, a connector too close to a panel edge may interfere with tooling. Identifying the conflict before fabrication allows your team to adjust the design or agree on suitable tooling.

Each finding should identify the affected location, explain the concern, and provide an actionable recommendation. Approved changes should then appear in the files used for production.

What Is the Satellite PCB Assembly Process?

Satellite PCB assembly follows a sequence of engineering review, material preparation, placement, soldering, post-processing, and verification.

satellite PCB assembly, https://www.bestpcbs.com/blog/2026/10/satellite-pcb-assembly/
  1. Manufacturing-file review PCB files, the BOM, placement data, drawings, and special requirements are checked. Manufacturing questions are returned for clarification before preparation proceeds.
  2. Material verification PCB and component identity, condition, quantities, and documentation are inspected. Shortages, discrepancies, and proposed substitutions require resolution.
  3. Production preparation Stencils, placement programs, supports, and instructions are prepared against the approved revision. Moisture-sensitive materials receive the required handling.
  4. Paste printing and placement Paste deposits and initial placements are checked as specified. First-piece inspection confirms component identity, polarity, orientation, and critical positions.
  5. Soldering and mixed assembly SMT components follow the approved reflow process. Through-hole components and connectors are installed using the selected soldering method.
  6. Post-processing Required cleaning, staking, coating, hardware installation, and programming follow the assembly instructions, preserving access for intermediate checks.
  7. Final inspection and delivery Boards complete the agreed inspections and tests. Defects are resolved, relevant checks are repeated after repair, and accepted assemblies are packaged with the specified records.

How Are Satellite PCB Assemblies Inspected and Tested?

Inspection checks manufacturing quality; electrical and functional testing verify specified circuit behavior. Your plan should cover critical connections and functions before integration restricts access.

Solder paste inspection

SPI measures specified paste characteristics, such as volume and alignment, before placement. It helps detect printing conditions that may cause bridging or insufficient solder.

AOI and visual inspection

AOI examines accessible features, including placement, polarity, and visible solder conditions. Visual inspection supports checks of connectors, hardware, handling damage, staking, and coating.

X-ray inspection

X-ray examines selected hidden solder features beneath packages such as BGAs and QFNs. Define inspected locations, acceptance criteria, and required image records.

Electrical and functional testing

ICT or flying probe can check accessible connections and selected component values. Functional testing applies specified firmware, power, signals, and loads.

A power board may be checked for output voltage and protection response. A controller may be tested for startup, communications, and sensor interfaces.

Results should identify the tested board or batch and show the applicable limits and outcomes. After repair, repeat the inspections and tests affected by the work.

How Is Full Traceability Maintained Throughout Satellite PCB Assembly?

Full traceability links each delivered board or batch to its design revision, materials, manufacturing history, verification results, and approved changes.

satellite PCB assembly, https://www.bestpcbs.com/blog/2026/10/satellite-pcb-assembly/

Records connect through work orders, batch numbers, or individual serial numbers. The required detail depends on your hardware and acceptance needs.

  • Build identity: PCB revision, BOM revision, assembly drawings, and firmware version.
  • Material history: PCB manufacturing batch, component part numbers, and required supplier or lot information.
  • Production history: Relevant instructions, program identification, and completion records for specified operations.
  • Verification results: Inspection reports, X-ray records, electrical measurements, and functional-test results.
  • Changes and repairs: Approved substitutions, deviations, affected units, repair details, and retest results.

If a component lot requires investigation, these links help identify the assemblies containing it. If a unit fails testing, its history supports comparison with other boards.

Agree on record contents, product identification, delivery format, and retention period before production.

What Affects Satellite PCB Assembly Cost and Lead Time?

Cost and lead time depend on PCB construction, component availability, assembly complexity, testing, and documentation.

Board construction and assembly

Materials, layer count, copper thickness, vias, finish, and tolerances affect fabrication cost. Fine-pitch parts, double-sided assembly, mixed technologies, coating, and mechanical installation can add preparation and processing time.

Component supply

Long-lead devices, approved-source restrictions, screening, and minimum purchase quantities affect procurement. An early BOM review helps you identify schedule constraints and consider approved alternatives.

Testing and records

Fixtures, programming adapters, functional-test development, additional inspection, serialization, and reporting require separate preparation. Their inclusion should be visible in the quotation.

Order quantity

Stencils, tooling, and engineering setup contribute more to the unit price of a small initial build. Repeat orders may reuse suitable preparation when the design and requirements remain consistent.

Compare quotations using the same materials, processes, tests, records, and packaging. Delivery estimates should reflect component readiness and completion of the required tooling and test inputs.

Why Choose EBest Circuit as Your Satellite PCB Assembly Manufacturer?

EBest Circuit coordinates PCB fabrication, sourcing, assembly, and engineering support through a dedicated project team.

  • Resolve manufacturing concerns early: File review identifies package, panel, and assembly issues while your team can still make practical changes.
  • Coordinate PCB and PCBA requirements: Fabrication and assembly needs are reviewed together, reducing mismatched assumptions about materials, mechanical features, and files.
  • Retain control over component changes: Procurement follows the approved BOM and sourcing requirements, with proposed alternatives submitted through the agreed approval process.
  • Verify critical board features: Inspection and testing can address hidden joints, connectors, power sections, and specified functions.
  • Plan the records needed for acceptance: Traceability and reporting requirements are discussed before production and included in the agreed delivery.
  • Simplify technical communication: Engineers familiar with your project help resolve questions across purchasing and manufacturing.

Looking for a satellite PCB assembly partner? Send your Gerber files, BOM, assembly drawings, quantities, and reliability and traceability requirements to sales@bestpcbs.com. EBest Circuit’s engineering team can review manufacturing needs, component availability, and inspection and testing requirements before preparing a quotation.

What Files Are Needed for a Satellite PCB Assembly Quote?

Provide PCB manufacturing data, the BOM, placement files, assembly drawings, quantities, and test requirements.

  • Board and assembly files: Gerber or ODB++, drill data, fabrication drawings, stackup, BOM, pick-and-place data, and assembly drawings.
  • Manufacturing requirements: Materials, workmanship specifications, cleaning, coating, staking, mechanical installation, and traceability.
  • Programming and testing: Firmware, programming method, procedures, operating conditions, pass/fail limits, fixtures, and required reports.
  • Order details: Hardware purpose, quantities, target delivery, customer-supplied materials, packaging, and destination.

Contact EBest Circuit for a satellite PCB assembly quote. Send your Gerber files, BOM, assembly drawings, quantities, and testing and traceability requirements to sales@bestpcbs.com. Our engineering team will review your manufacturing needs and component availability to prepare a project-specific quotation.

FAQ About Satellite PCB Assembly

Q1: Can an NDA be arranged before complete design files are shared?

A1: Request NDA review before disclosure so confidentiality terms can be agreed before detailed files are exchanged.

Q2: Can several population variants be included in one order?

A2: Yes, provided each variant has clearly identified BOM, placement, assembly, and test requirements.

Q3: What happens to unused customer-supplied components?

A3: Return, storage, or disposal arrangements should be agreed before production begins.

Q4: Can packaging protect sensitive connectors or protruding components?

A4: Packaging can be specified around the assembly’s mechanical features, handling needs, and transport requirements.

Q5: Can part of an order be delivered before the remaining quantity?

A5: Staged delivery can be evaluated against material readiness, production scheduling, and completion of the required acceptance checks.

Q6: Does requesting a quotation commit the project to production?

A6: A quotation supports technical and commercial evaluation, with production proceeding after order acceptance and manufacturing release.

You may also like

Pump Controller PCB for Reliable Water Pump Operation

October 10th, 2026

A pump controller PCB receives operating signals and controls when a water pump starts, stops, or changes speed. Its role depends on the system: a tank-filling controller responds to water level, a pressure booster responds to demand, and a variable-speed pump may need a power stage as well as control logic. These boards share a purpose, but they are not interchangeable.

For a pump-control assembly, reliable production involves both the low-voltage signal circuitry and the connections that carry or switch power. EBest Circuit supports PCB fabrication, component sourcing, assembly, inspection, and agreed functional testing from customer-approved designs. To discuss a pump controller PCB build, contact sales@bestpcbs.com.

pump controller PCB
Representative pump controller assembly; AI-generated conceptual image.

What Does a Pump Controller PCB Control?

The board turns operating inputs into pump commands. Depending on its design, those commands may switch a relay, energize an external contactor, or set the speed of a motor drive.

Pressure, level, or flow input → control logic → switching or drive command → pump response

Feedback closes this loop. For example, a filling system can start a pump at a low tank level and stop it at a high level. An alarm input may override the normal command when a monitored fault occurs.

The PCB is the bare board; the PCBA includes its mounted components. A complete controller may also include firmware, terminals, a display, and an enclosure. Some control boards only send signals to a separate power unit. Others integrate a motor control PCB function and carry motor current through onboard switching devices.

How Do On/Off and Variable-Speed Pump Controllers Differ?

On/off control changes whether a pump runs; variable-speed control changes how fast it runs. This difference changes both the control method and the power electronics.

Control type Board output Pump behavior
On/off control A relay or control signal switches the pump supply or an external contactor. The pump starts and stops as operating thresholds are reached.
Variable-speed control A speed command goes to a separate drive, or an onboard power stage drives a compatible motor. The system adjusts speed within its operating range to follow demand.

A controller with a speed-setting input does not necessarily contain the motor power stage. Conversely, a low-voltage brushless pump assembly may combine sensing, control, and three-phase switching on one board.

Variable-speed control can help regulate pressure as demand changes, but it requires a compatible pump and motor-drive system. Adding a PWM output to an on/off controller does not make an ordinary fixed-speed pump suitable for variable-speed operation.

pump controller PCB
Representative relay-control and integrated motor-drive architectures; actual boards vary by design.

How Do Pressure, Level, and Flow Signals Affect Pump Operation?

Each signal describes a different part of the water system. A controller may use one signal for normal operation and another to detect an abnormal condition.

  • Pressure: Indicates system pressure. A pressure drop can trigger a booster pump; a pressure-feedback loop can also adjust speed.
  • Level: Indicates how much water is available or stored. Low and high levels can define a filling or draining cycle.
  • Flow: Indicates water movement. It can help distinguish an active demand from a condition in which the motor runs but water is not being delivered.

The input circuit must match the sensor interface. A float switch provides a switching state; a transmitter may provide an analog signal such as 4–20 mA. These inputs need different conditioning and cannot be substituted simply because both measure a water-system condition.

The same level signal can produce opposite actions. A low level may start a tank-filling pump, while a low source-water level may stop it to prevent dry running.

How Does a Pump Controller Detect Dry Running and Motor Overload?

Dry-running protection detects insufficient water; overload protection detects excessive motor loading. One does not automatically provide the other.

Condition Possible detection method Key limitation
Dry running Source-level or suction-pressure monitoring; combined pressure and flow monitoring; a suitable motor-load detection method. The method must suit the pump. Loss of water does not necessarily cause high current.
Motor overload or stall Current monitoring, thermal protection, or driver fault detection. Thresholds and timing must distinguish a fault from permitted starting behavior.

Some pump systems infer loss of water from reduced motor load. Others use a dedicated level switch or evaluate pressure and flow together. A current sensor alone does not establish that a board has effective dry-running protection.

After detection, the controller may stop the pump, signal an alarm, and either wait for a manual reset or follow a defined restart sequence. The restart behavior is part of the protection design; repeated attempts without restored water availability can keep exposing the pump to the original problem.

Why Does a Pump Start and Stop Too Frequently?

Frequent cycling can originate in the water system, the control settings, or the feedback signal. Replacing the PCB will not correct a leak or restore a pressure tank’s lost precharge.

  • Pressure falls after shutdown: A leak or water returning through an ineffective check valve can repeatedly create a new start demand.
  • Very little water is drawn between starts: In a system using a pressure tank, tank condition, sizing, and precharge can affect cycling.
  • Start and stop thresholds are close: Small changes in pressure or level may repeatedly cross both thresholds.
  • The reported signal fluctuates: Sensor noise or an unstable connection can create switching commands that do not reflect actual demand.

Separate start and stop thresholds provide hysteresis: the pump does not change state at one identical boundary in both directions. Filtering or timing logic may also suppress brief disturbances, where the application permits it. These measures cannot replace a required fault response or repair a hydraulic problem.

How Can Motor Switching Disrupt Pump Controller Signals?

Switching currents can disturb the supply and reference voltages used by the controller. A board may read its sensors correctly while idle, then show unstable readings or reset when the motor starts.

Motor-drive switching loops, relay circuits, and long external wiring can couple disturbances into nearby signal paths. If a sensitive input shares an unsuitable return path with a pulsed power current, the input’s reference can move even when the sensor output has not changed.

Relevant PCB layout measures include:

  • Keeping high-current switching loops compact and away from sensitive input routing.
  • Placing decoupling and driver components close to the pins they support.
  • Routing current-sense connections separately from load-current paths where the sensing arrangement requires it.
  • Providing controlled return paths and appropriate filtering or protection at external interfaces.

Ground-plane splits are not a universal solution; a split can force signal return current onto a longer path. Layout should follow the selected driver and interface requirements. Functional testing should include switching activity and representative inputs, rather than only checking that the board powers on.

How Do Moisture and Condensation Affect Pump Controller PCBs?

Moisture can reduce surface insulation and contribute to corrosion. Contamination on the board can make the effect worse, producing leakage currents or intermittent behavior before visible damage appears.

A controller can encounter condensation inside its housing even without direct splashing. Protection therefore involves the assembly surface as well as the enclosure.

  • Conformal coating: Protects covered surfaces, but performance depends on cleanliness, coverage, cure, and material suitability.
  • Potting: Surrounds the assembly with a larger volume of protective material. Material choice affects heat transfer, mechanical stress, and repairability.
  • Enclosure protection: Addresses exposure through the housing and cable entries. A coated board alone does not establish an enclosure’s waterproof rating.

Connector contacts, test points, and other designated areas may need to remain uncoated. The finished assembly needs evaluation under its intended environmental conditions; applying a protective layer is not, by itself, proof of long-term moisture resistance.

pump controller PCB
Representative board and enclosure protection; this image does not establish an ingress-protection rating.

FAQs About Pump Controller PCBs

Can one pump controller PCB operate different pumps?

Only within its supported electrical and control range. Motor type, starting current, output stage, sensor interfaces, and control settings all affect compatibility.

Is matching the supply voltage enough when replacing a board?

No. Connector pinouts, motor outputs, sensor inputs, firmware, and protection behavior also need to match. Two boards with the same voltage rating can perform different functions.

Does every pump controller PCB need firmware?

No. Some simple controllers use analog or fixed logic circuits. A microcontroller-based board needs suitable firmware, while some motor-control ICs use configurable built-in functions.

Does a successful power-on test prove the controller works?

No. It does not demonstrate correct sensor response, pump commands, or fault handling. The agreed test scope should exercise those functions with suitable input simulation and loads.

What is the difference between ordering a bare PCB and a PCBA?

A bare PCB provides the circuit’s physical interconnections. A PCBA includes assembled components; programming and functional testing are additional operations that must be included in the manufacturing scope when required.

For a pump controller PCB project, EBest Circuit can review the approved board data and assembly requirements, with particular attention to power connections, sensor interfaces, and the agreed test sequence. Discuss your build with sales@bestpcbs.com.

You may also like

Solar Panel PCB Board Manufacturer with Turnkey Solutions

October 9th, 2026

A solar panel PCB board manages charging, power conversion, protection, sensing, and communication in solar controllers, inverters, lighting, and monitoring equipment.

This article examines board selection, materials, environmental protection, manufacturing, testing, cost, supplier evaluation, and the prototype-to-production transition.

Solar Panel PCB Board, assembled solar control PCB on an engineering workbench

What can make a solar PCB quotation unreliable?

  • You receive quotes for different boards: Charge controllers, inverter boards, lighting controllers, and monitoring boards require different components, copper, assembly processes, and tests.
  • Important costs appear later: Missing voltage, current, battery, cooling, coating, connector, or environmental requirements can change materials, assembly, and testing.
  • The production board differs from the prototype: Unreleased rework, substitutions, firmware, or fixture changes can return as repeat-order problems.

EBest Circuit builds PCBs and PCBAs for solar controllers, inverters, lighting, and monitors. One quotation can cover parts purchasing, fabrication, SMT/THT assembly, firmware programming, and board-level testing.

  • Know what is missing before purchasing: You receive a list of conflicts or open items across the PCB data, BOM, assembly files, mechanics, programming, and tests.
  • Keep one approved build identity: Your BOM, PCB revision, work instructions, firmware, and test limits stay connected throughout production.
  • Repeat the approved result: Accepted substitutions, rework, firmware changes, and test updates are added to the released package for the next order.

Ready for a quotation? Send your current files, quantity, and delivery destination to sales@bestpcbs.com. You will receive a proposed manufacturing scope and a clear list of any information still needed.

What Is a Solar Panel PCB Board?

A solar panel PCB board is the printed circuit assembly inside a solar controller, inverter, light, monitor, or battery-powered product. It carries the components and copper connections used to manage power and system functions.

In a charge controller, the board regulates panel input and battery charging. In an inverter, it supports switching, sensing, protection, and communication. In solar lighting, it can manage charging, LED output, timing, and motion sensing.

The photovoltaic panel generates DC power. The PCB receives, converts, measures, or controls that power inside the equipment. State the equipment and board function in the RFQ so the manufacturer can quote the correct construction, components, assembly process, and tests.

What Types of PCB Boards Are Used in Solar Panel Systems?

Solar systems commonly use charge-control, inverter power, lighting-control, and monitoring or communication boards. Larger products may divide these functions across several PCBAs.

Board Type Main Function Typical Equipment Fit
Charge-control board Regulates panel input, battery charging, load control, sensing, and protection MPPT or PWM controllers, battery chargers, off-grid power units
Inverter power board Converts variable DC power into controlled AC power and manages switching, sensing, and protection Solar inverter PCB assemblies, microinverters, and power-conversion units
Lighting-control board Charges a battery and controls LEDs, timers, dimming, motion sensing, or dusk-to-dawn operation Solar streetlights, garden lights, signs, and remote lighting products
Monitoring or communication board Measures voltage, current, temperature, and status while transferring data to a local or remote system Combiner monitoring, trackers, gateways, remote sensors, and energy-management equipment

How Do You Choose a Solar Panel PCB Board for Your Application?

Match the board to the equipment specification. Start with maximum panel input, battery system, continuous and peak current, required controls, connector interfaces, cooling, and the mounting envelope.

  • Input and battery limits: State normal and maximum panel voltage, battery chemistry, nominal battery voltage, charging method, reverse-polarity behavior, and expected fault conditions.
  • Load and conversion task: Define continuous current, peak or inrush current, output type, switching frequency where relevant, duty cycle, and allowed temperature rise.
  • Control and communication: List sensing accuracy, protection logic, firmware ownership, programming interface, CAN, RS-485, Ethernet, wireless, or other required connections.
  • Mechanical fit: Provide board outline, mounting holes, connector positions, cable direction, height limits, heatsink or chassis contact, and keep-out areas.
  • Operating environment: Identify ambient temperature, humidity, condensation, dust, vibration, enclosure sealing, cleaning, and coating requirements.

Use an off-the-shelf module when its electrical limits, interfaces, dimensions, compliance evidence, and lifecycle fit the product. Use custom manufacturing for unique mechanics or functions, controlled parts and tests, owned design data, and repeat orders.

Which PCB Materials Are Suitable for Solar Electronics?

Use standard FR4 when the board’s temperature, electrical stress, current density, insulation, and assembly requirements stay within its limits. It is a practical choice for many charge-control, lighting, and monitoring boards.

Choose high-Tg FR4 when the expected board temperature or assembly profile needs more thermal margin. Confirm the actual laminate grade and Tg in the quotation instead of accepting a generic “high-temperature material” description.

Use metal-core, ceramic, or heavy-copper construction only when the power or heat path requires it. Ask the manufacturer to confirm routing, isolation, soldering, inspection, cost, laminate, copper, layers, holes, and finish before approval.

How Can Solar Panel PCB Boards Handle Heat and Outdoor Exposure?

Provide the expected current, component losses, maximum ambient temperature, and available cooling. The manufacturer can then check copper areas, thermal vias, interface materials, heatsink or chassis contact, and airflow against your operating conditions.

For outdoor use, state the expected condensation, humidity, dust, salt, UV, and temperature cycling. Specify enclosure and connector protection, spacing, drainage, cleaning, and coating, then verify the prototype under the intended load and environment.

How Are Solar Panel PCB Boards Manufactured and Assembled?

Your approved release should follow the order from file review through fabrication, sourcing, SMT/THT assembly, inspection, programming, and testing. Resolving file conflicts first helps you avoid buying components or tooling against the wrong revision.

  1. Close the file questions: Confirm Gerber or ODB++, drill files, stackup, drawings, netlist, BOM, placement data, polarity, mechanics, quantities, and test requirements.
  2. Fabricate the approved PCB: Build the specified stackup, holes, copper, solder mask, surface finish, and profile, then complete electrical and dimensional checks.
  3. Prepare approved parts and firmware: Verify manufacturer part numbers, allowed alternates, moisture handling, firmware, and programming instructions before kitting.
  4. Assemble and inspect the PCBA: Place and solder SMT and THT parts, then inspect polarity, placement, joints, cleanliness, and mechanical support.
  5. Receive a revision-linked build record: Keep programming, test results, rework, substitutions, inspection findings, and disposition tied to the board you ordered.

Use the prototype build to confirm the soldering sequence, support for heavy magnetics and connectors, manual operations, and inspection access. Approved findings can then become part of the repeat-production instructions.

Solar Panel PCB Board, mixed SMT and through-hole assembly inspection for a solar power PCBA

What Tests Should a Solar Panel PCB Board Pass?

Your test plan should show what each check proves and what result you will receive. Specify bare-board electrical test, assembly inspection, firmware programming, functional checks, fixtures, loads, pass limits, and the required record.

  • Charge-control board: Check programmed identity, power-up current, input and output behavior, battery-interface logic, sensing, communications, and agreed protection responses using approved limits.
  • Inverter power board: Add insulation-related checks, gate-drive verification, current and voltage sensing, controlled-load operation, temperature observations, and protection tests appropriate to the design.
  • Monitoring board: Focus on sensor accuracy, analog stability, interface protection, communication, firmware version, low-power behavior, and data integrity.
  • Assembly workmanship: Use visual inspection or AOI for visible joints and placement; apply X-ray only where hidden joints or the risk profile justify it.

Use the board-level results to confirm that the PCBA is ready for product integration. Complete-system validation still needs your actual panel, battery, enclosure, wiring, cooling, firmware, EMC and safety requirements, and intended operating environment.

Solar Panel PCB Board, controlled board-level functional testing on a solar electronics PCBA

How Much Does a Custom Solar Panel PCB Board Cost?

Compare quotations only when they cover the same revision, quantity, component responsibility, test coverage, and delivery terms. Otherwise, the lowest price may represent a smaller manufacturing scope.

PCB cost follows size, panel use, layers, laminate, copper, drilling, line and space, finish, tolerances, inspection, and quantity. PCBA adds components, sourcing risk, tooling, placement, SMT/THT work, programming, coating, fixtures, testing, packaging, and specified reports.

Ask for separate one-time, bare-board, component, assembly, programming, testing, packaging, and freight charges. You can then see which costs recur, which items are optional, and which supplier has omitted work you still need.

How Do You Choose a Solar Panel PCB Board Manufacturer?

Choose the manufacturer that gives you the clearest control over cost, revisions, quality, and delivery. Send each supplier the same files and compare the answers and evidence returned with the quotation.

  • A quote matched to your files: Look for confirmation of the stackup, copper, spacing, drill, finish, tolerances, panel conditions, and any special processes that affect price or lead time.
  • One plan for mixed assembly: Confirm how the supplier will handle SMT, THT, selective or manual soldering, heavy parts, connectors, cleaning, coating, and mechanical support.
  • No substitution without your approval: Require manufacturer part numbers, alternate-part rules, and written approval before a material or component change enters the build.
  • Test coverage you can verify: Agree on electrical test, inspection, programming, fixture ownership, functional limits, result format, and the boundary between PCBA testing and system validation.
  • Records you can retrieve: Put the required lot, panel, or serial-number level in your PCB assembly traceability requirements, together with the material, process, firmware, test, rework, and shipment fields you need.
  • A delivery date with clear dependencies: Separate material lead time, fabrication, assembly, testing, approval, shipping, and Incoterm so you know what can change the schedule.

Why Choose EBest Circuit for Solar Panel PCB Board Manufacturing?

Working with EBest Circuit can reduce the handoffs between purchasing, PCB fabrication, assembly, programming, and testing. You send one controlled package and receive one quoted scope for the work EBest will perform.

  • Fewer quotation surprises: A combined file review exposes conflicts among fabrication data, assembly files, parts, mechanics, programming, and tests before materials are committed.
  • More control over component changes: Purchasing follows your approved part numbers and alternate rules, with proposed substitutions sent back for approval when product performance or fit could change.
  • Fewer revision mismatches: PCB construction, BOM, packages, polarity, firmware, and SMT/THT instructions remain tied to the same released build.
  • A smoother move beyond the prototype: Approved rework, part changes, firmware, fixture updates, and test limits can be added to the package before pilot or repeat production.
  • Clear test responsibility: The quotation can state the included inspections, programming, functional checks, customer inputs, fixtures, limits, and result format.
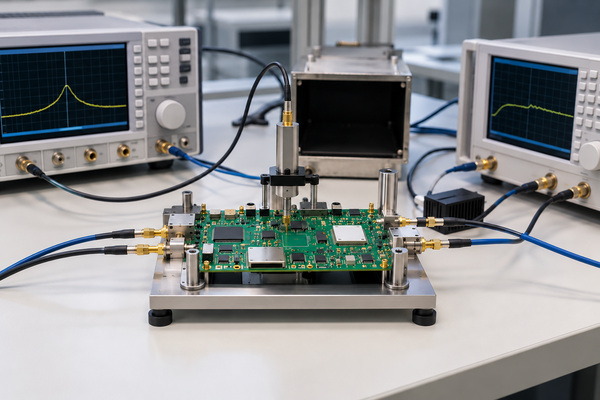
  • Traceability that fits your order: You can define the material, production, firmware, inspection, test, rework, and shipment records you need, plus how they should be retrieved.
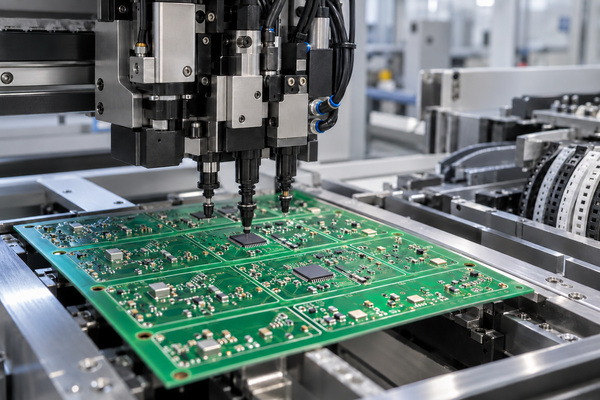
You can review the included work, customer-supplied inputs, open decisions, and exclusions before placing the order. This gives your engineering and purchasing teams a common basis for approving cost, schedule, and responsibility.

What Files Are Required for a Custom Solar Panel PCB Board Quote?

You can request a quotation before every detail is final. Send the latest files you have, mark open items clearly, and EBest can return the missing information that affects price, lead time, or manufacturability.

  • PCB files: Gerber or ODB++, drill files, stackup or fabrication drawing, board outline, material, copper, thickness, finish, and quantity.
  • Assembly files: BOM with manufacturer part numbers, pick-and-place data, assembly drawings, polarity notes, and any customer-supplied parts.
  • Programming and test: Firmware and programming instructions, plus the test method, fixture information, operating conditions, limits, and required result format.
  • Order details: Prototype or production quantity, mechanical or coating requirements, delivery destination, required date, packaging, labeling, and traceability needs.

FAQs About Solar Panel PCB Boards

Q1: Can one PCB design support both 12 V and 24 V battery products?

A1: Only when the input range, charging method, component ratings, sensing scale, protection thresholds, thermal behavior, and firmware are designed and validated for both systems. Do not treat a voltage-label change as proof of compatibility.

Q2: Can one PCB revision be assembled with several firmware variants?

A2: Yes, if each variant has a controlled firmware identifier, programming instruction, configuration record, label, and test profile. The finished board must remain traceable to the exact software loaded.

Q3: Is a physical sample enough to reproduce an existing solar control board?

A3: A sample can support inspection, but it rarely defines internal copper, materials, tolerances, approved components, firmware, or test limits. Repeat production should use controlled design and manufacturing data.

Q4: Which changes require another prototype build?

A4: Rebuild and revalidate when a change can affect power conversion, protection, thermal behavior, isolation, component fit, firmware interaction, mechanical integration, or test coverage. Documentation-only corrections may not require a new build.

Q5: How should returned boards be prepared for failure analysis?

A5: Record the board identity, operating conditions, symptoms, event history, firmware, photos, and any work already performed. Avoid cleaning, reworking, or powering the board again unless the analysis plan calls for it.

Q6: Can spare boards be included with a production order?

A6: Yes, but define whether they are finished assemblies, unprogrammed units, or bare PCBs and how they will be packaged, labeled, stored, and tested. Spare units should remain tied to the same approved revision.

Conclusion

A clear solar panel PCB board package gives you comparable prices, visible responsibilities, and a smoother production transfer. Define the function, operating conditions, materials, assembly, tests, quantity, and delivery requirements before approving the supplier.

Send your current Gerber or ODB++, stackup, BOM, assembly data, quantity, test needs, and delivery destination to sales@bestpcbs.com. EBest Circuit will return a proposed turnkey scope and the questions needed to complete your quotation.

You may also like