PCB manufacturing PCB manufacturing
Home > Blog

VGA Connector: Pinout, Types and PCB Design

November 6th, 2026

A vga connector is a 15-contact, three-row D-sub interface that carries analog video between equipment and a display. It transmits separate red, green and blue signals, synchronization signals and, on DDC-compatible equipment, display-identification data. It does not carry standard audio. The familiar blue port is usually a female receptacle; a cable plug normally has male pins.

For a replacement or custom PCB, matching the connector’s appearance is only the beginning. Pin numbering, mounting dimensions and signal conversion determine whether the connection works. A VGA plug cannot become an HDMI interface through a simple change of wiring.
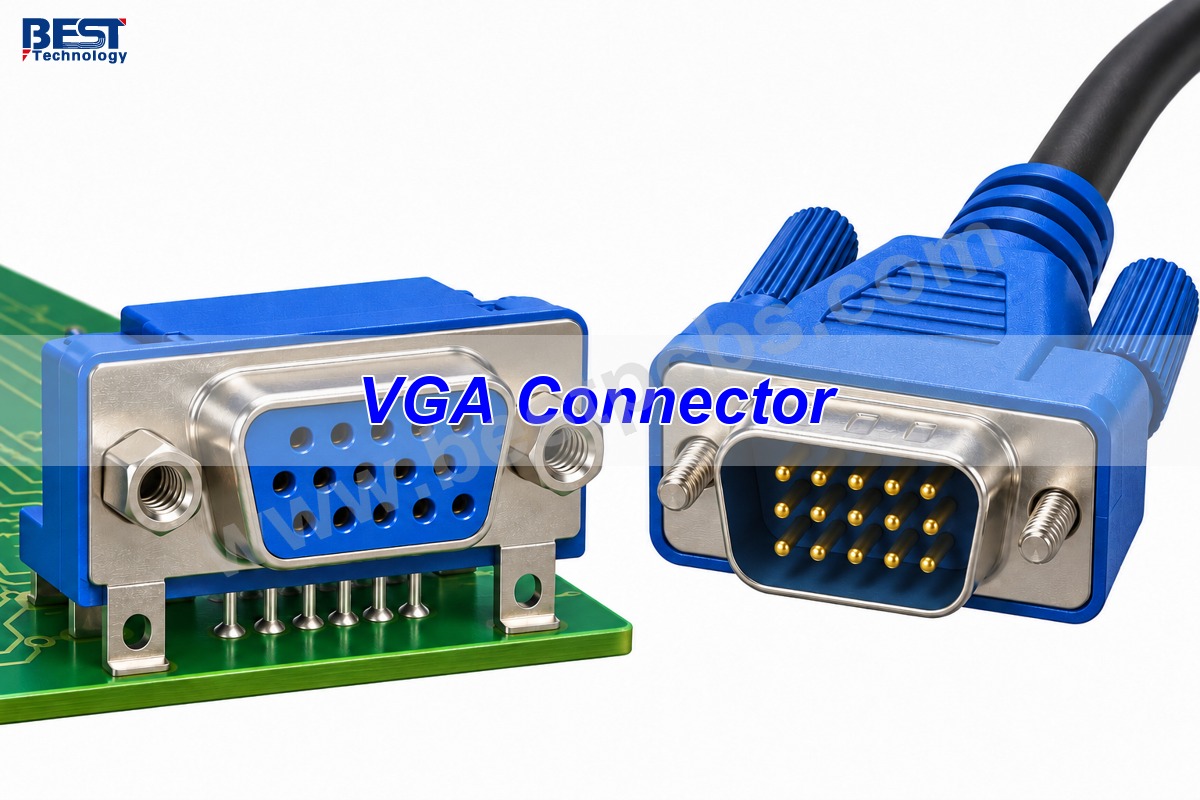
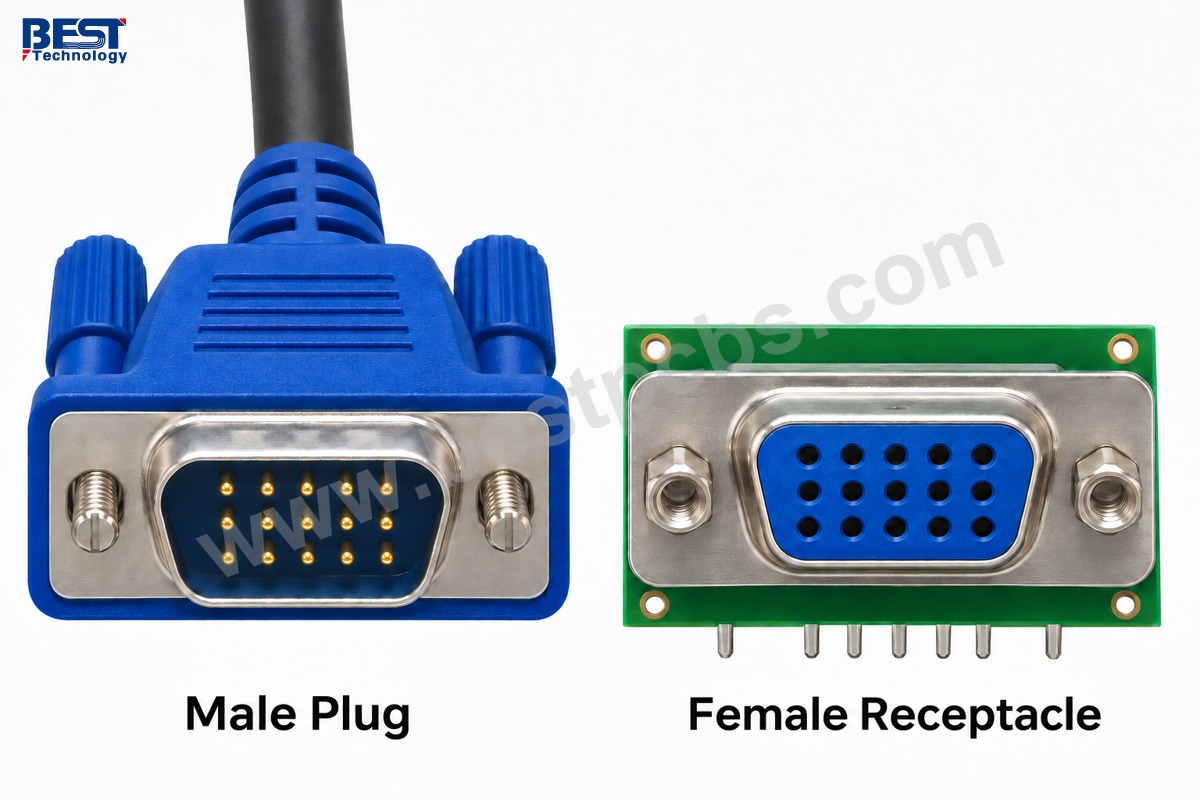
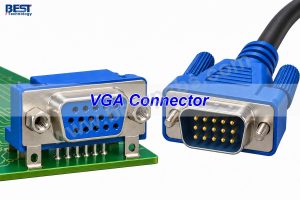
VGA male cable plug beside a female board-mounted receptacle

Key Takeaways

  • Standard VGA uses 15 contacts in three rows, commonly called DE-15, HD-15 or high-density D-sub.
  • RGB occupies pins 1–3; horizontal and vertical sync use pins 13 and 14.
  • Connector mating-face and solder-side views are mirrored. A footprint must follow the selected part’s drawing.
  • VGA carries analog video, while HDMI carries digital video and audio. Conversion requires active electronics.
  • RGB routing, connector anchoring and shell grounding need separate design checks.
  • Continuity testing cannot verify image quality; a functional display test is also needed.

What Does a VGA Connector Look Like?

A VGA connector has a D-shaped metal shell surrounding three rows of five contacts, with screw fasteners on either side.

The D shape helps prevent reversed insertion, while the screws keep a cable seated. Blue insulation is common but not mandatory. Count the contacts rather than identifying a port by color: a two-row, nine-contact D-sub connector is not the standard 15-contact VGA interface.

At EBest Circuit, we support the PCB and assembly around display interfaces. Our PCB assembly service can combine component sourcing, board assembly and the agreed inspection or functional test. For a VGA design, the exact connector part number connects the mechanical drawing, footprint and assembly plan.

VGA Connector Types

VGA connector types differ by contact gender, mounting direction and termination method, while retaining the familiar 15-contact mating interface.

Type Physical arrangement Typical use
Male cable plug 15 projecting pins Connecting a cable to an equipment port
Female PCB receptacle 15 socket contacts with board tails Computer, controller or display interface board
Right-angle PCB connector Mating axis parallel to the PCB Rear-panel or enclosure-edge port
Vertical PCB connector Mating axis perpendicular to the PCB Top-entry connections
Solder-cup connector Wire-termination cups at the rear Custom cable and panel assemblies
VGA male plug and female receptacle with three rows of contacts

Gender does not establish video direction: a port’s circuit determines whether it is an input or output. Similarly, two right-angle receptacles can share the same mating face but have different board-hole positions, shell supports or connector heights. Do not substitute one footprint for another without checking the drawing.

VGA Connector Pinout

The VGA connector pinout assigns pins 1–3 to analog RGB, pins 6–8 to their returns, and pins 13–14 to horizontal and vertical synchronization.
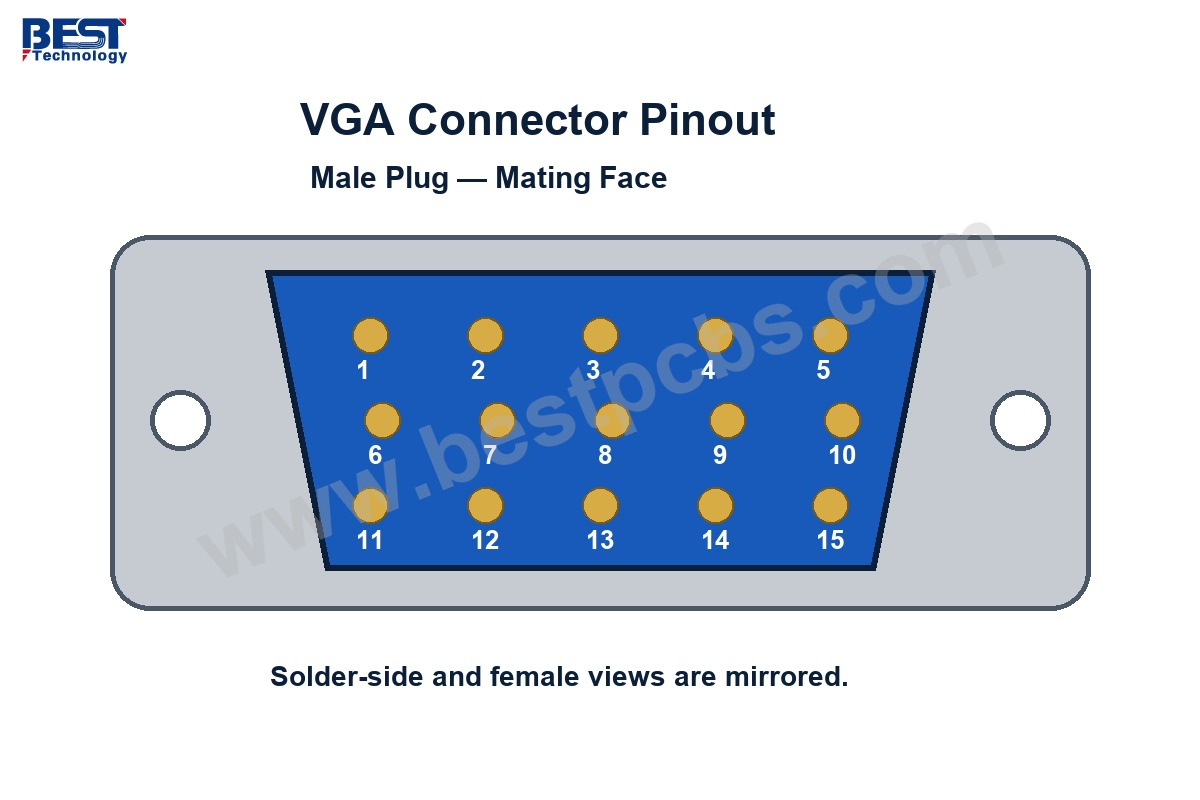
Male VGA plug mating-face pin numbering with three rows of five contacts
Pin Common signal assignment
1 Red video
2 Green video
3 Blue video
4 Legacy ID / reserved; equipment-specific
5 Ground / equipment-specific detection
6 Red return
7 Green return
8 Blue return
9 DDC supply on supported implementations; check equipment specification
10 Sync ground
11 Legacy ID / reserved / ground; equipment-specific
12 DDC data, SDA
13 Horizontal sync
14 Vertical sync
15 DDC clock, SCL

DDC means Display Data Channel. It allows the source to read the display’s identification and supported timing information. Older VGA implementations used some auxiliary contacts differently, so the table is not a substitute for the equipment schematic.

The drawing above shows the male plug’s mating face, not its solder side. A female mating-face view is mirrored. Identify pin 1 from the connector drawing before wiring a cable or releasing a PCB footprint.

What Is a VGA Connector Used For?

VGA connects an analog video source to a compatible monitor or projector, especially in existing computers, industrial equipment and installed display systems.

Keeping VGA can make sense when a product must work with an established display. It avoids replacing a functioning monitor solely because a new controller has been introduced. For a new digital-only system, however, adding VGA also means providing analog-video circuitry or a suitable converter.

VGA is not restricted to the original 640 × 480 graphics mode. Higher resolutions are possible, but the connector itself does not guarantee a maximum resolution or refresh rate. The source, monitor, cable quality and analog bandwidth must support the selected timing.

How Does a VGA Connector Compare with HDMI?

VGA sends analog video without standard audio; HDMI sends digital video and can also carry audio.

Feature VGA HDMI
Video signaling Analog RGB with synchronization Digital
Audio in the interface No Supported
Common full-size connector 15-contact D-sub 19-contact Type A
Conversion between formats Active conversion required
Typical reason to use it Compatibility with an existing analog display Digital display connection

On an LCD monitor, a digital connection avoids converting a digital source into analog video and then sampling it back into digital form. With VGA, poor cable performance or sampling adjustment can soften text or produce ghosting. HDMI is usually the more straightforward choice when both devices support it natively.

Can You Connect VGA to HDMI with a Passive Adapter?

No. VGA-to-HDMI requires an active converter because analog RGB must be sampled and encoded as digital video.
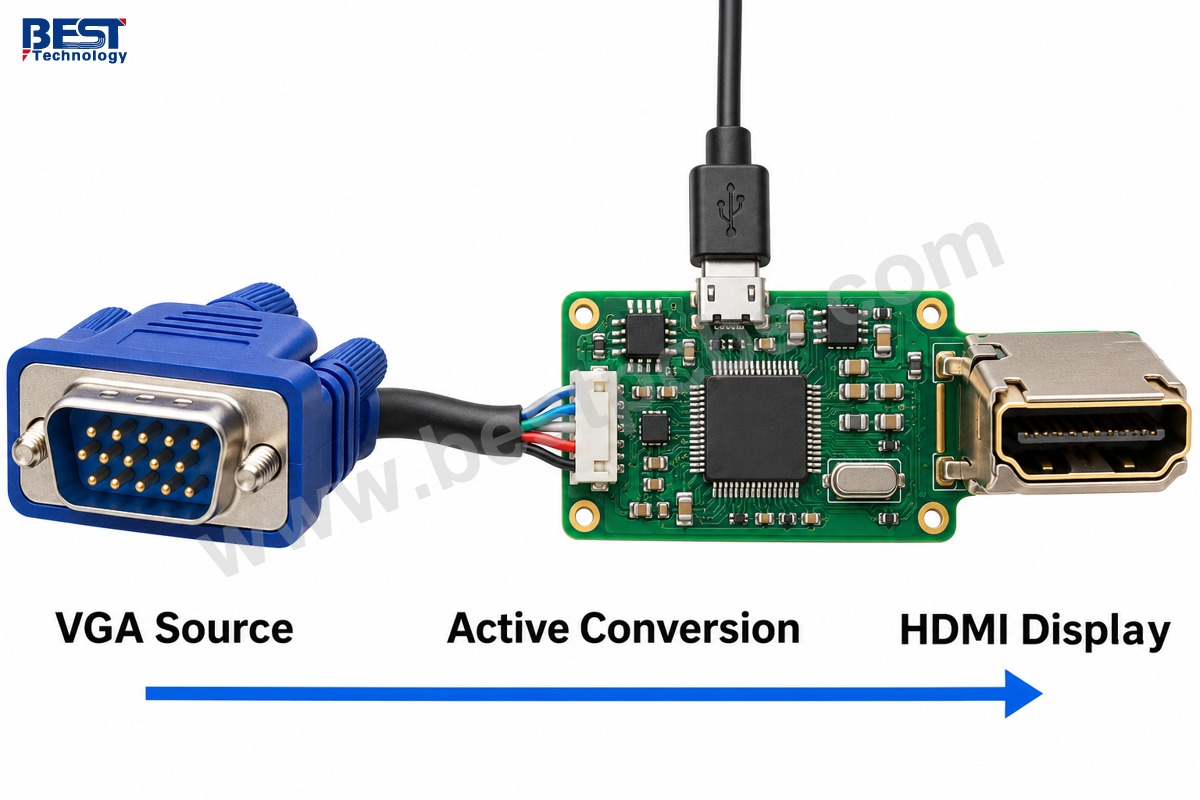
VGA source connected through an active conversion board to an HDMI display

For the reverse direction, an HDMI to VGA connector adapter needs digital-to-analog conversion. An adapter can look like a short cable yet contain active electronics inside its housing. Direction matters: a converter intended for an HDMI source and VGA monitor is not automatically reversible.

  • Match the converter’s input to the source and its output to the display.
  • Check its supported resolution and refresh rate.
  • Provide external power when the converter requires it.
  • Use a separate audio input if a VGA-to-HDMI converter must add audio.

DVI-I is a different case: a source that actually provides analog video through its DVI-I port can use a passive VGA adapter. A digital-only DVI-D source cannot supply that analog signal through passive rewiring.

What Matters When Routing VGA Signals on a PCB?

VGA PCB routing needs controlled RGB paths, continuous return references and a connector footprint matched to the selected component.

As a concrete example, NXP’s PTN3355 layout guideline routes the RGB traces to the VGA connector at 75 Ω. That is a design-specific reference, not a reason to assign 75 Ω to every contact. The sync and DDC circuits follow their own driver, receiver and protection requirements.

  • RGB routing: follow the video device’s impedance and termination network; avoid unnecessary stubs and reference-plane interruptions.
  • Protection: place suitable low-capacitance protection near the exposed connector, following its datasheet layout.
  • DDC: check voltage compatibility, pull-ups and the intended supply arrangement rather than treating SDA and SCL as video traces.
  • Mechanical fit: confirm the mating axis, panel opening, mounting hardware and board-edge position.

Our PCB design support can help connect the stackup and footprint review with fabrication requirements. Trace width alone does not establish impedance: dielectric thickness, copper geometry and the reference structure also affect it.

VGA Connector Soldering

VGA connector soldering must produce reliable electrical joints while its mounting features absorb cable insertion and screw-loading forces.
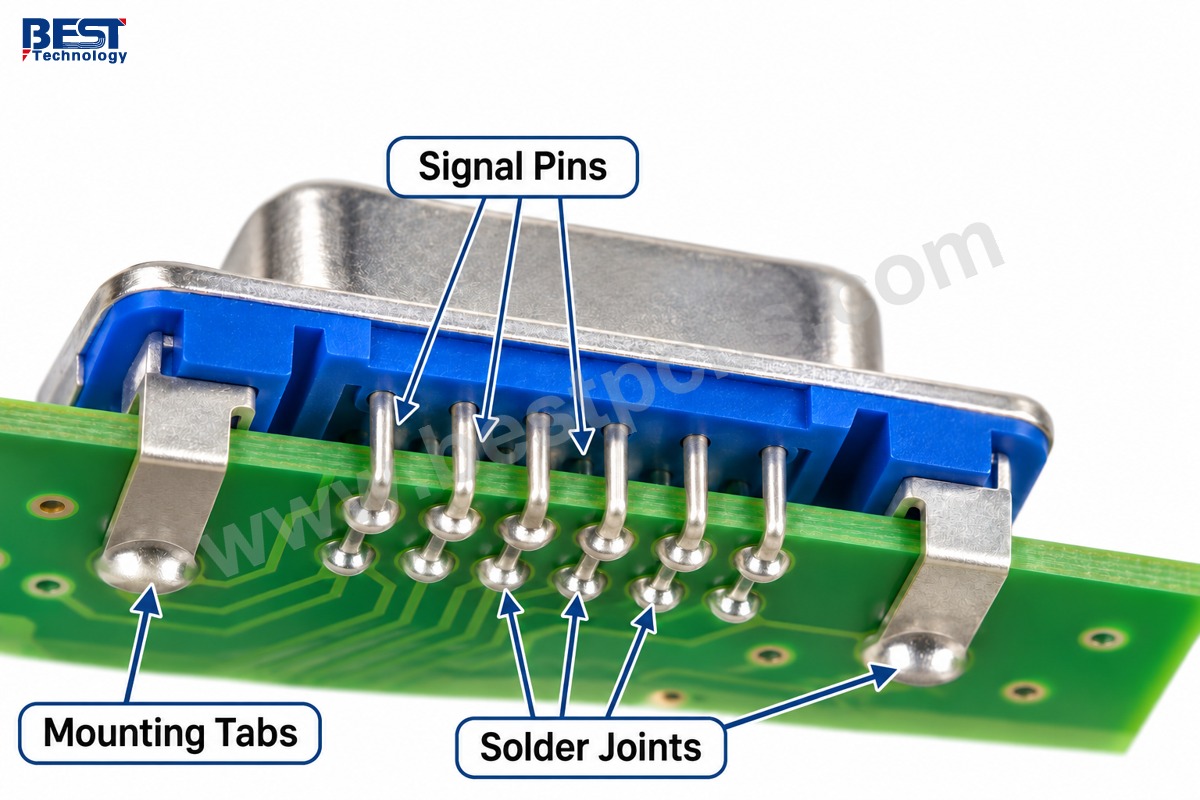
VGA PCB connector signal pins mounting tabs and solder joints

Many board-mounted parts use through-hole tails, although other termination styles exist. The soldering method depends on the connector’s process rating and the assembly design. A plastic housing rated for one process must not be assumed suitable for another.

  • Inspect signal pins for bridges, incomplete wetting and damaged pads.
  • Check that mounting tabs and jack hardware are fitted as specified.
  • Verify connector seating and alignment with the enclosure.
  • Inspect shell-to-ground connections against the approved EMC design.

At EBest Circuit, we include the connector drawing and agreed inspection criteria in the assembly review. Signal-pin solder joints should not be the only support for a cable that receives repeated handling.

How Do You Troubleshoot a VGA Connection?

Start with the display’s selected input, cable seating and supported video timing before assuming the PCB has failed.

  1. Confirm the signal path. Verify source output, monitor input and any converter’s direction and power.
  2. Substitute a known-good cable. Inspect for bent or recessed contacts with the equipment powered down.
  3. Choose a supported timing. Use the monitor and converter specifications, not a connector label.
  4. Separate the symptom. A missing color suggests an RGB path fault; unstable synchronization and failed display detection involve different circuits.
  5. Test the assembly. After connectivity checks, verify color channels, synchronization and display detection with the intended display.

Continuity checks must be performed on disconnected, unpowered hardware. A continuity result does not prove analog bandwidth or picture quality. For a production test, define the display timing and visible pass/fail pattern instead of accepting any image as sufficient.

FAQs About VGA Connectors

Is DE-15 the same as DB-15?

The familiar three-row VGA connector is properly described as DE-15 or HD-15. It is often sold as DB-15, but that name can also cause confusion with a different two-row D-sub. Confirm the contact layout.

Can a USB-C port drive a VGA monitor?

Yes, with a compatible active adapter and a USB-C source that supports the adapter’s required display mode. A USB-C connector alone does not guarantee video output. USB graphics adapters are a separate product category with their own requirements.

Does a VGA cable carry sound?

No. Standard VGA carries video and associated control signals. Some cable assemblies add a separate audio lead, but that sound does not travel through the standard VGA contacts.

Is there one maximum VGA cable length?

No single length guarantees a usable picture at every timing. Cable construction, shielding, analog bandwidth and equipment performance affect the result. Validate the intended cable length at the actual operating resolution.

Will a passive VGA splitter create two independent desktops?

No. It cannot create an additional graphics output or independent image. A suitable distribution amplifier can send the same video to multiple displays; separate desktops require a source architecture that supports multiple outputs.

Need a PCB Assembly with a VGA Interface?

A dependable VGA interface combines the correct pinout, a mechanically sound connector and a verified analog-video path. These checks belong in the design and assembly plan, not only in final troubleshooting.

For a custom controller or display-interface board, send the connector part number and project requirements to sales@bestpcbs.com. We can review PCB fabrication, assembly and the functional checks needed for your build.
You may also like

What Is Mainboard? Meaning, Parts and Device Types

November 6th, 2026

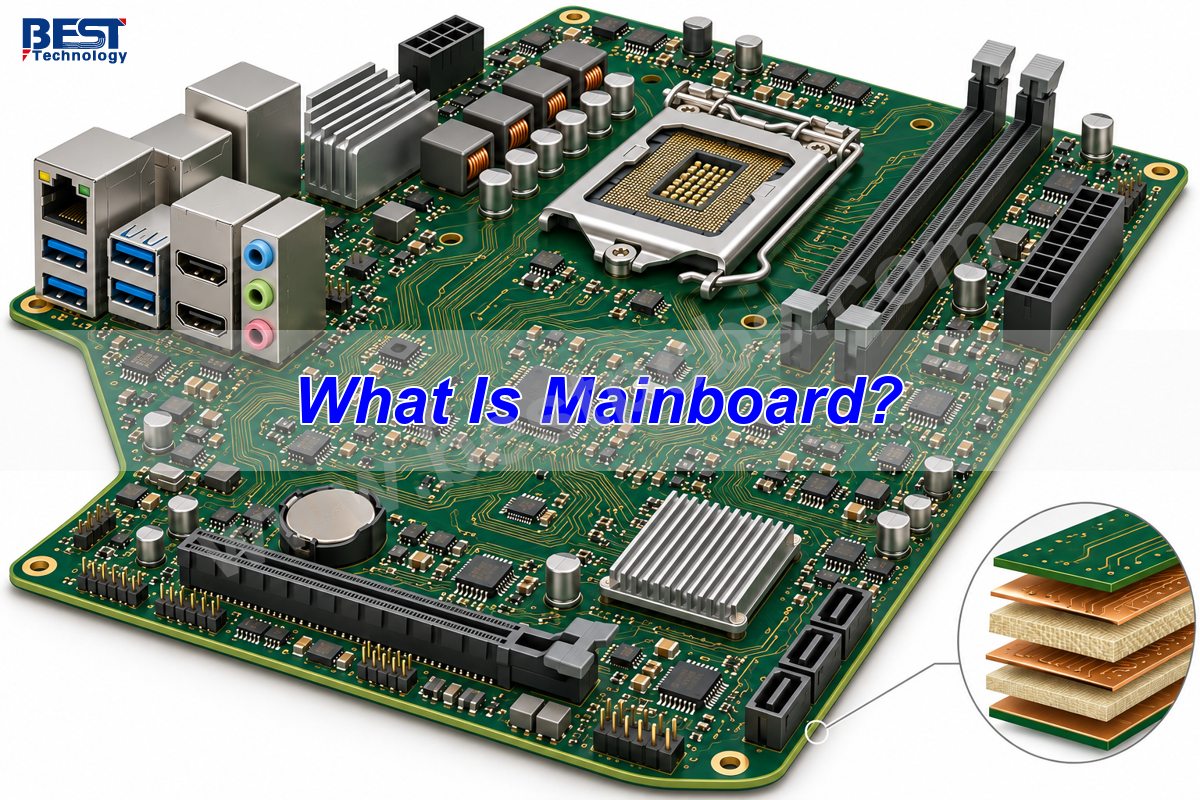
A mainboard is the primary assembled circuit board in an electronic device. It connects the processor, memory, power circuits and interfaces so the device can operate as one system. In a desktop computer, it is usually called a motherboard; in a laptop, phone or television, it may be called a system board, logic board or main board. These names describe its role, not one standard shape or circuit design.

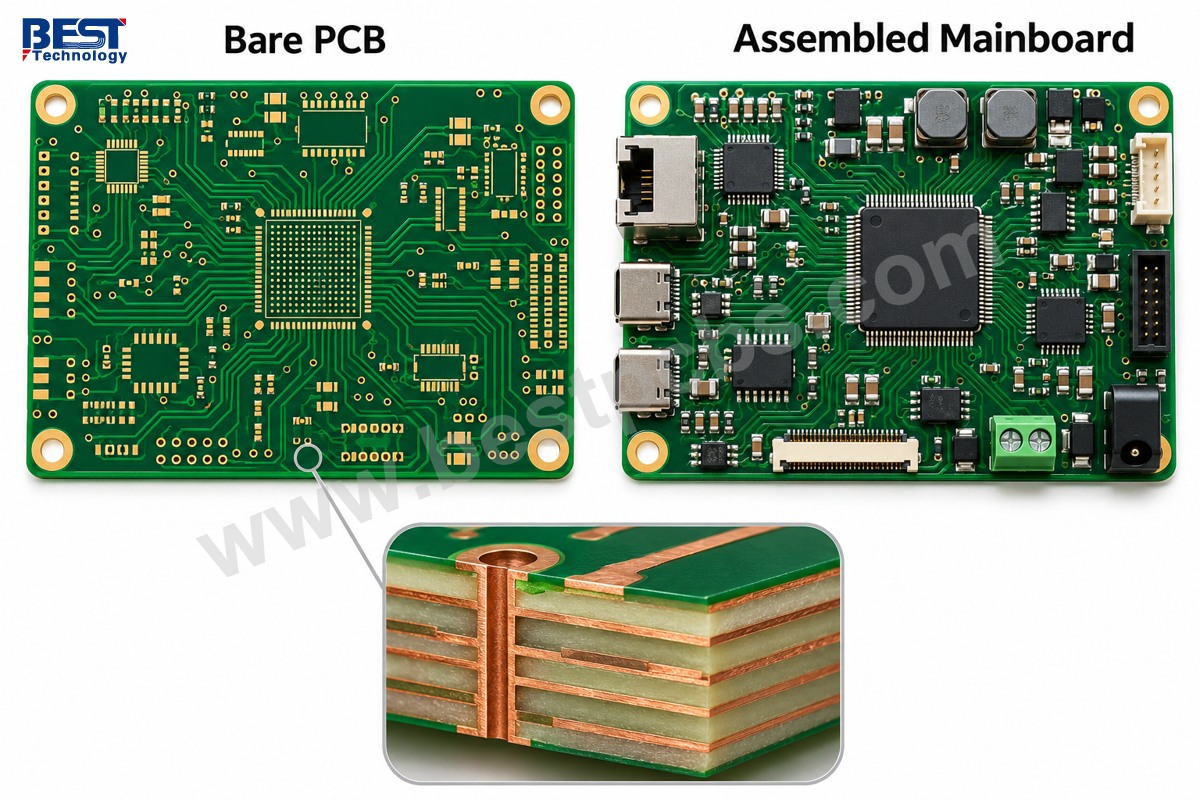
The important distinction is between the board’s function and its construction: a mainboard is a working electronic assembly, while a bare PCB is the unpopulated platform on which that assembly is built.

Three-dimensional desktop mainboard and multilayer PCB structure

Key Takeaways

  • A mainboard is the device’s primary circuit assembly, not the processor itself.
  • Mainboard and motherboard usually mean the same thing in a computer, but device-specific board names vary.
  • Desktop boards often use removable processors and memory; laptop and phone boards frequently integrate these parts through soldered packages.
  • ATX and Mini-ITX describe desktop form factors, not universal mainboard sizes.
  • A matching outline is not enough for replacement: board revision, firmware, connectors and component compatibility also matter.
  • Custom mainboards require both PCB manufacturing checks and assembly-level functional validation.

Is a Mainboard the Same as a Motherboard?

Yes—in a computer, mainboard and motherboard normally identify the same primary system board. Neither term specifies a particular processor, memory generation or board size.


Term Meaning Common context
Mainboard / motherboard Primary populated system board Computers and electronic equipment
System board / logic board Alternative names for the primary board Service manuals and integrated devices
Bare PCB Fabricated board without installed components PCB manufacturing
Daughterboard Secondary board connected to the mainboard Port modules, expansion and auxiliary functions
Backplane Board interconnecting plug-in modules Modular equipment and rack systems


A device may contain several PCBs but only one primary control board. A separate charging-port board or display interface board does not become the mainboard simply because it is essential to operation. For a closer look at PC-specific hardware, see our guide to motherboard components and PCB structure.

At EBest Circuit, we support custom PCB fabrication and PCB assembly. For a mainboard project, we review the released board design, component packages and assembly requirements together; manufacturing a bare board and delivering a functioning system assembly are different scopes of work.

What Does a Mainboard Do?

A mainboard provides electrical connections, power distribution and control interfaces between the device’s major components.

  • Data paths: copper traces carry signals between processors, memory, storage and peripheral interfaces.
  • Power delivery: regulators convert incoming power into the rails required by individual circuits, while capacitors help control local voltage variation.
  • Startup support: reset, clock and firmware circuits establish the conditions needed for the processor to begin executing code.
  • External connections: connectors link the board to displays, sensors, networks, controls and other equipment.

The processor executes instructions; the mainboard makes its connections and supporting circuits available. A board does not independently increase processor speed, and a connector’s presence alone does not guarantee a particular interface speed.

What Parts Are on a Mainboard?

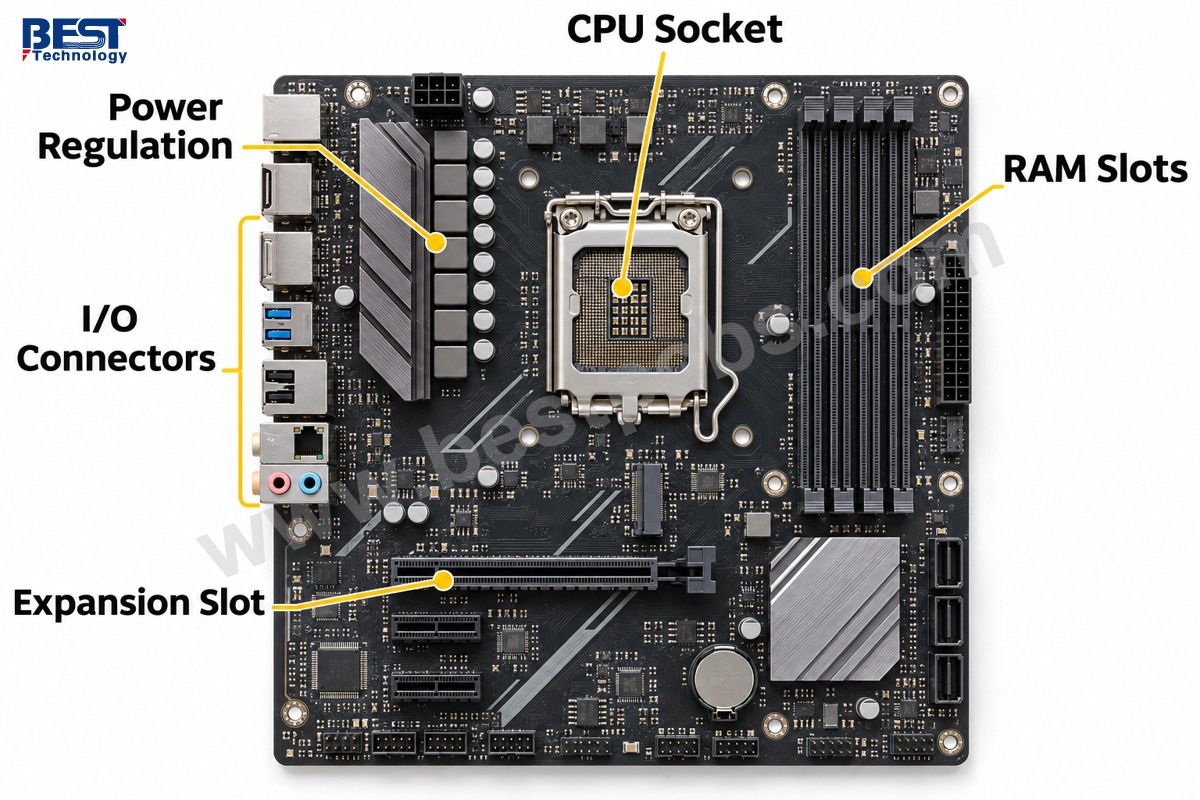
A mainboard typically contains a processor or processor connection, memory connections, power regulation, clock circuitry, firmware storage and I/O interfaces.

Desktop mainboard showing CPU socket RAM slots power regulation expansion slot and I/O connectors

On a desktop board, these features are relatively easy to recognize: a CPU socket, long DIMM memory slots, PCIe expansion slots and rear-panel connectors. Storage may connect through M.2 sockets or cable connectors. The voltage-regulator area commonly includes inductors, switching devices and capacitors near the processor.

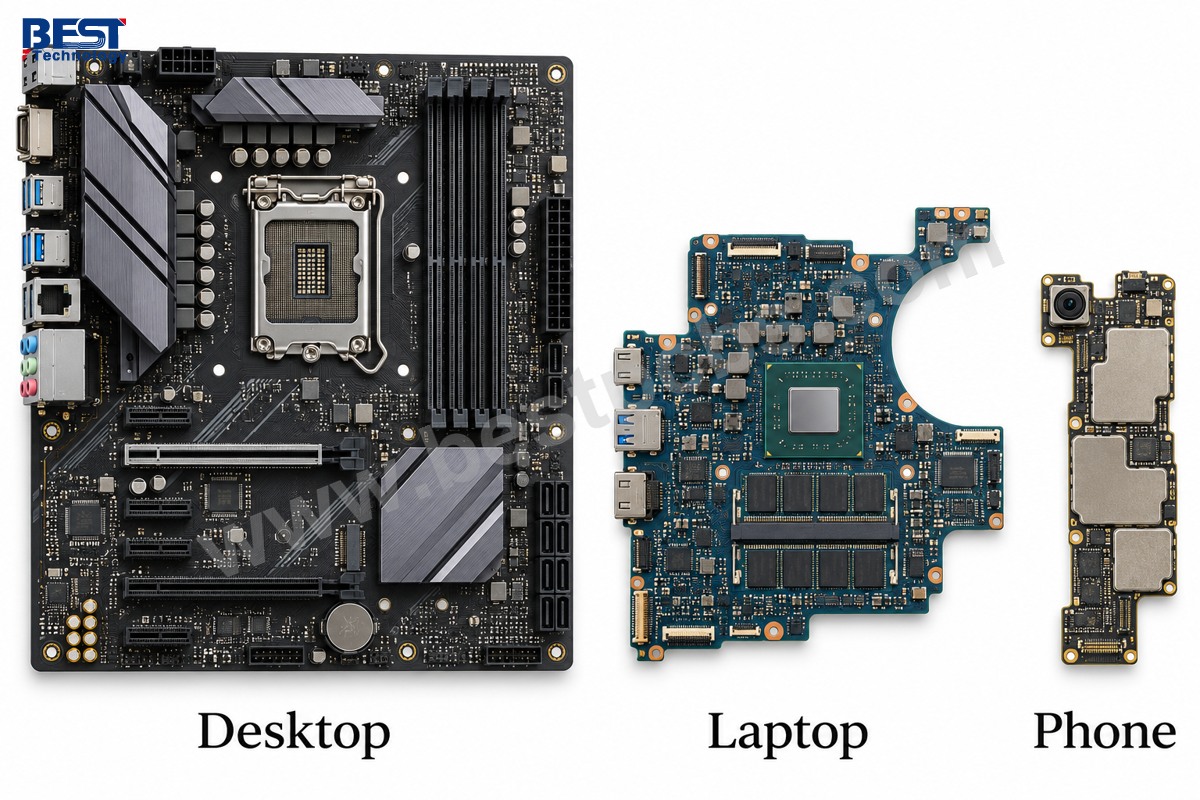
A phone mainboard looks different. Its processor, memory and storage often use soldered packages, while metal shields cover sensitive sections. Smaller board-to-board or flex connectors replace many of the large sockets found on a desktop. Not every mainboard has a separate chipset, removable battery or expansion slot.

How Do Mainboards Differ Between Devices?

Mainboards differ primarily in integration, mechanical layout, power requirements and the interfaces needed by the host device.


Device Typical board arrangement Main design priority
Desktop PC CPU socket, memory slots, expansion connectors Compatibility and expansion
Laptop Model-specific outline, compact connectors, often soldered processor Space, battery operation and cooling
Smartphone Dense IC assembly, shielded sections, flex connections Integration and RF coexistence
Television Video processing and panel/network interfaces Display compatibility and signal processing
Industrial controller Processor, field interfaces and application-specific I/O Required operating environment and dependable interfaces
 
 
Desktop laptop and phone mainboards with different physical layouts

In a television, the mainboard usually handles video, audio and system control; the power supply and panel timing functions may reside on separate boards. In industrial equipment, an I/O board can remain separate from the processor board to support different sensor or actuator connections. The product architecture determines the division.

Which Types of Motherboard Have Standard Sizes?

Common desktop types of motherboard include ATX, microATX and Mini-ITX; laptop, phone and many industrial mainboards instead use product-specific outlines.


Desktop form factor Nominal board dimensions
ATX 305 × 244 mm
microATX Up to 244 × 244 mm
Mini-ITX 170 × 170 mm


These dimensions describe board format, not electrical compatibility. An ATX board can still require a different CPU socket, memory type or firmware than another ATX board. Check the exact manufacturer’s drawing for mounting positions, connector locations and component clearances rather than choosing by the size label alone.

What Is the Motherboard Made Of?

A typical motherboard uses a multilayer glass-reinforced epoxy PCB with patterned copper conductors, plated connections, solder mask and installed electronic components.

Bare multilayer PCB compared with a populated mainboard assembly

FR-4 is a common material family, but it is not one fixed laminate grade. High-speed interfaces may require a lower-loss material selected against the actual signal path. Copper layers carry signals and distribute power; dielectric layers separate conductors; plated vias connect selected layers. The green surface is usually solder mask, not the bulk insulating material.

There is no universal mainboard layer count or thickness. For a custom board, stackup selection must account for routing density, reference planes, impedance, mechanical fit and fabrication capability. Our PCB design support connects these board-level decisions with manufacturing review.

Where Is Motherboard Located?

In a desktop PC, the motherboard is mounted inside the case on chassis standoffs; in a laptop or phone, it sits inside the enclosure beneath covers, shields or cooling parts.

The desktop CPU cooler, memory modules and expansion cards attach to it, making it the largest central connection board in many conventional PCs. A laptop board may occupy only part of the base because the battery, speakers and cooling system take the remaining space. Device service documentation is the safest identification reference; do not open a powered device or a television power-supply area to locate a board.

What Is My Mainboard Model?

On a Windows PC, open System Information with msinfo32 and read BaseBoard Manufacturer, BaseBoard Product and BaseBoard Version under System Summary.

  1. Press Windows + R, enter msinfo32 and press Enter.
  2. Record the BaseBoard fields and the system manufacturer/model.
  3. Compare those details with the device’s official support documentation.
  4. For replacement, confirm the physical part number and revision through the service manual or a qualified technician.

Firmware-provided fields can be generic or incomplete. A laptop’s marketing model is not always its mainboard part number, and one product family may contain several board revisions. Phone and TV replacements additionally need the correct regional variant, display compatibility and firmware configuration. A visually similar board is not sufficient evidence of interchangeability.

What Manufacturing Checks Matter for a Custom Mainboard?

A custom mainboard needs checks for PCB connectivity, component assembly and actual system operation; none of those stages replaces the others.

  • Before fabrication: confirm connector orientation, mounting holes, stackup, controlled-impedance requirements, solder-mask clearances and access for testing.
  • During assembly: check component identity and polarity, stencil deposits and placement; inspect solder joints using methods appropriate to the packages. Hidden BGA joints may require X-ray inspection.
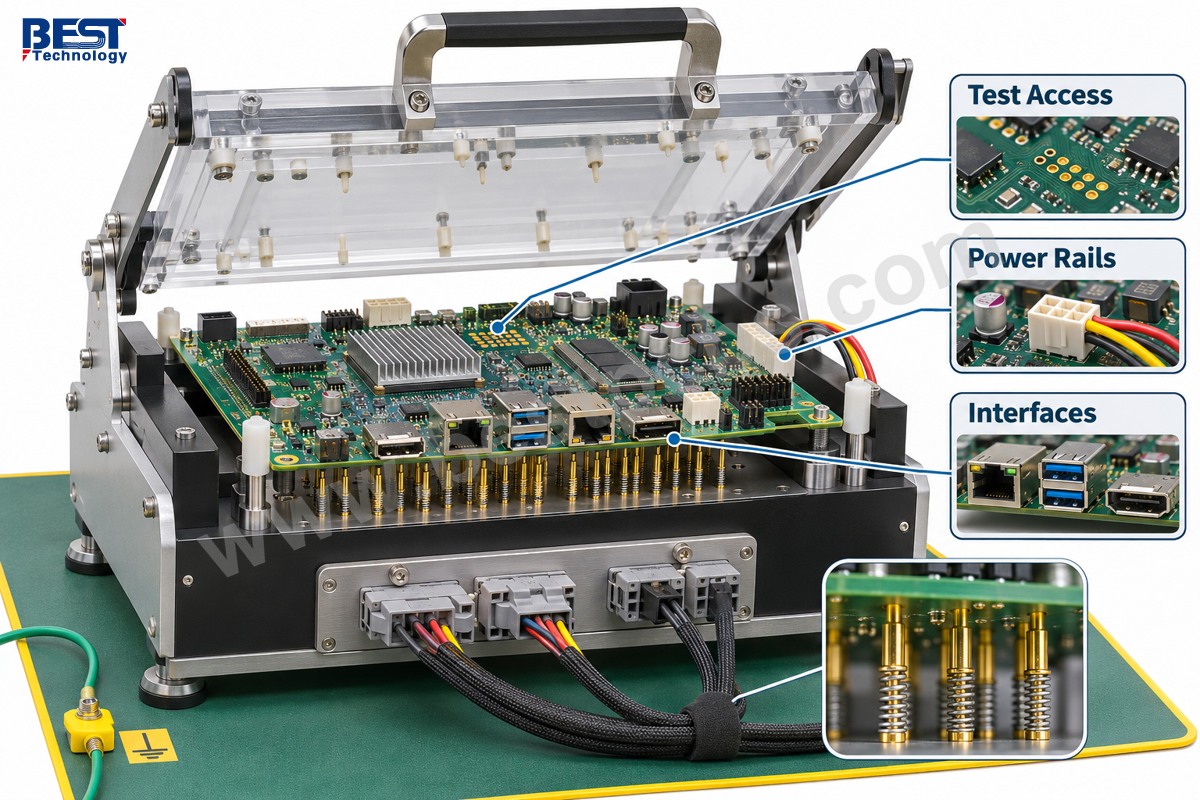
  • During validation: measure specified power rails, verify startup and firmware loading, and exercise required interfaces with defined pass/fail limits.
Industrial mainboard in a fixture showing test access power rails and interfaces

A PCB electrical test can detect opens and shorts in the fabricated interconnect, but it cannot establish that an assembled board boots or communicates correctly. Likewise, a successful boot does not prove every interface works. At EBest Circuit, we align the manufacturing review and agreed inspection scope with the customer’s assembly and test requirements rather than treating a populated board as a finished, validated product by default.

FAQs About Mainboards

Is a mainboard a CPU?

No. The CPU is the processor; the mainboard is the circuit assembly that connects it to memory, power and interfaces. The processor may be socketed or soldered.

Can a mainboard be replaced without changing every component?

Sometimes. Desktop parts may be reusable when the socket, memory, firmware and power connections match. Highly integrated laptop and phone boards require device-specific compatibility checks.

Does a black screen prove the mainboard has failed?

No. A display, cable, power supply, memory fault or firmware issue can produce similar symptoms. Diagnosis must isolate the fault before replacing the board.

What is mainboard firmware?

It is low-level software stored for the board’s startup and hardware-control functions. PCs commonly use UEFI firmware; embedded devices can use different bootloaders and firmware architectures.

Is every mainboard a single-board computer?

No. A single-board computer integrates the core computing functions on one board. A desktop mainboard commonly still requires separately installed memory, storage and other parts to form a usable system.

From Mainboard Design to a Working Assembly

A mainboard is defined by its central system role, not by one shape, layer count or processor family. For a custom product, the useful next step is to connect the mechanical layout, circuit design and validation plan before production begins.

If you are developing a custom mainboard, contact our engineering team at sales@bestpcbs.com to discuss PCB fabrication, assembly and the inspection or functional testing your project requires.

You may also like

ESP32 C3 vs S3: Key Differences, Performance and Power

November 4th, 2026

ESP32 C3 vs S3 is a comparison between a compact, cost-focused wireless controller and a more capable processor for demanding connected devices. The C3 suits many sensors, switches and simple control products, while the S3 offers more processing capacity, expanded memory options and interfaces for displays, cameras and USB applications. Both support 2.4 GHz Wi-Fi and Bluetooth Low Energy, so the biggest differences lie beyond basic wireless connectivity.

At EBest Circuit (Best Technology), we provide PCB fabrication, component sourcing and PCB assembly services for customers bringing electronic products into production. For an ESP32-based board, the selected chip or module affects the footprint, component list and assembly requirements. To discuss manufacturing your C3- or S3-based PCB assembly, contact sales@bestpcbs.com.

ESP32 C3 vs S3

ESP32 Comparison Chart: C3 vs S3 Specifications

The ESP32-S3 has more computing and interface resources; the ESP32-C3 provides a simpler platform when those extras are unnecessary. The table compares chip specifications, rather than the features of a particular development board.

Specification ESP32-C3 ESP32-S3
Main CPU Single-core, 32-bit RISC-V Dual-core, 32-bit Xtensa LX7
Maximum CPU clock 160 MHz 240 MHz
On-chip SRAM 400 KB, including 16 KB used for cache 512 KB
RTC SRAM 8 KB 16 KB
Wi-Fi 2.4 GHz, IEEE 802.11b/g/n 2.4 GHz, IEEE 802.11b/g/n
Bluetooth Bluetooth 5 LE Bluetooth 5 LE
USB controller functions USB Serial/JTAG USB Serial/JTAG and full-speed USB OTG
Chip-level GPIO count 16 or 22, depending on variant Up to 45
Chip package QFN32, 5 × 5 mm QFN56, 7 × 7 mm
Flash and additional RAM Flash configuration depends on part; no S3-style mapped PSRAM expansion Flash and PSRAM configuration depends on chip/module variant

Two distinctions matter when applying these figures to a board.

  • GPIO count is not the number of free application pins. Memory connections, reserved pins and board peripherals reduce the usable signals.
  • Chip size is not module size. The QFN dimensions exclude the module substrate, antenna and surrounding components.

ESP32-C3 vs ESP32-S3: CPU Performance and Maximum Speeds

The S3’s main advantage is more capacity for simultaneous work and demanding calculations. The C3 remains suitable for simpler workloads, such as reading sensors and periodically transmitting results.

Three aspects explain the performance difference.

  • Concurrent tasks. The S3’s two cores can share suitable workloads, such as interface updates and application processing. A single sequential task does not automatically run twice as fast; the benefit depends on how the firmware distributes work.
  • Numerical processing. The S3’s single-precision floating-point unit and SIMD instructions can help optimized signal-processing and selected machine-learning code. The software must use those resources, and the application must still fit its memory budget.
  • Time spent waiting. A task waiting on a sensor, memory transfer or network response may gain little from a higher CPU clock. Its slowest operation can remain the limiting factor.

A graphical interface processing audio while maintaining a network connection is therefore a stronger reason to use the S3 than a simple increase from 160 MHz to 240 MHz. CPU speed also does not establish wireless throughput; neither chip becomes a 5 GHz or Wi-Fi 6 device because its processor runs faster.

How Much Storage Does ESP32 Have? C3 vs S3 Memory Compared

The C3 has 400 KB of on-chip SRAM, while the S3 has 512 KB; flash and PSRAM capacities depend on the specific part. An advertised “8 MB” or “16 MB” figure needs a memory type beside it to be meaningful.

  • Flash holds firmware and persistent data. More flash can accommodate larger applications, graphics assets or files. Separate over-the-air update slots also need space alongside the running image and other partitions.
  • SRAM holds active working data. Stacks, variables and buffers use this memory while the application runs. A larger flash device does not fix a shortage of working RAM.
  • PSRAM adds working-memory capacity on supported S3 configurations. It is useful for larger image, display and audio buffers. Not every S3 module includes it, so the complete ordering code determines whether it is present.

For example, a camera application may fit its firmware in flash but still lack room for image buffers. A PSRAM-equipped S3 can address that capacity problem. External PSRAM uses an external interface and cache, however, so it does not behave like equally fast internal SRAM for every operation.

ESP32-C3 vs ESP32-S3: USB, GPIO and Peripheral Differences

The S3 offers more options for USB applications, displays and cameras. The C3 covers many simpler sensor and control interfaces, including SPI and I2C peripherals.

USB functions

  • C3 USB Serial/JTAG supports programming, console communication and debugging. Its fixed-function controller cannot be reprogrammed into a general-purpose USB keyboard or storage device.
  • S3 USB OTG supports device or host applications with suitable firmware and board hardware. It is full-speed USB, with 12 Mbit/s signaling, rather than 480 Mbit/s high-speed USB. Host operation also needs the appropriate power arrangement for the attached device.

Displays, cameras and available pins

  • S3 LCD and camera interfaces support products that need these dedicated connections alongside buttons and other peripherals.
  • C3 SPI or I2C connections can serve sensors and modest displays; a simple user interface does not automatically require an S3.
  • Module pin assignments determine which signals remain available. Flash or PSRAM connections occupy pins, and boot-strapping pins need appropriate conditions during startup.

The interface list is therefore only the starting point. The selected module’s pin map determines which functions can coexist on the finished board.

ESP32-C3 vs S3 Deep Sleep Current: Chip vs Board Power Consumption

The C3 has a lower listed baseline deep-sleep current, but that figure alone does not predict finished-product battery life. The retained functions and the rest of the board also consume power.

Device and state Typical chip current Conditions represented
ESP32-C3, deep sleep 5 µA RTC timer and RTC memory retained
ESP32-S3, deep sleep 7 µA RTC memory powered; RTC peripherals powered down
ESP32-S3, deep sleep 8 µA RTC memory and RTC peripherals powered

These are typical chip values under the stated configurations, not maximum limits or measured currents for complete boards.

Three parts of the operating cycle determine the result.

  • Sleep current from the complete board. Regulators, LEDs, memory, sensors and USB bridges may remain powered. One peripheral can outweigh the small difference between the two chips’ baseline figures.
  • Energy used during each wake-up. Startup, wireless connection and transmission all contribute. A product that reconnects frequently can spend a substantial part of its energy budget outside sleep.
  • Time spent active. Finishing a task sooner can sometimes offset a higher active current. This depends on the application and needs measurement.

Illustrative average-current calculation

Assume a board draws 100 mA for 1 second and 0.1 mA for the following 59 seconds.

Average current = (100 × 1 + 0.1 × 59) ÷ 60 ≈ 1.77 mA

These assumed currents are not measurements of either chip. The example shows why a full operating-cycle measurement is more useful than applying the lowest sleep figure to the entire battery-life calculation.

ESP32 C3 vs S3

ESP32 S3 vs C3: Which Features Are Worth the Extra Cost?

The S3 earns its place when its extra resources enable a required function or remove a bottleneck. For a simple connected sensor or relay controller, much of that capacity may remain unused.

Applications that can justify the S3

  • Camera products need enough working memory for image buffers and a suitable interface for the camera. A PSRAM-equipped S3 configuration can be valuable here.
  • Graphical interfaces benefit from memory for graphics and processing capacity for rendering while other tasks continue.
  • USB device or host products need an appropriate controller. In a suitable implementation, the S3’s OTG capability may avoid a separate USB controller.

Applications where the C3 may be sufficient

  • Sensors that wake periodically, collect a reading and transmit it.
  • Switches and relay controllers with modest processing demands.
  • Connected devices with a small display and limited buffering requirements.

Production cost also includes the surrounding hardware. A richer camera or display product may add memory, connectors and power circuitry, even when the processor integrates more functions.

Compare complete component lists delivering the same required functions. There is no fixed C3-to-S3 price gap across all module types, memory configurations, quantities and supply conditions. A bare C3 chip and a fully equipped S3 development board are not equivalent cost comparisons.

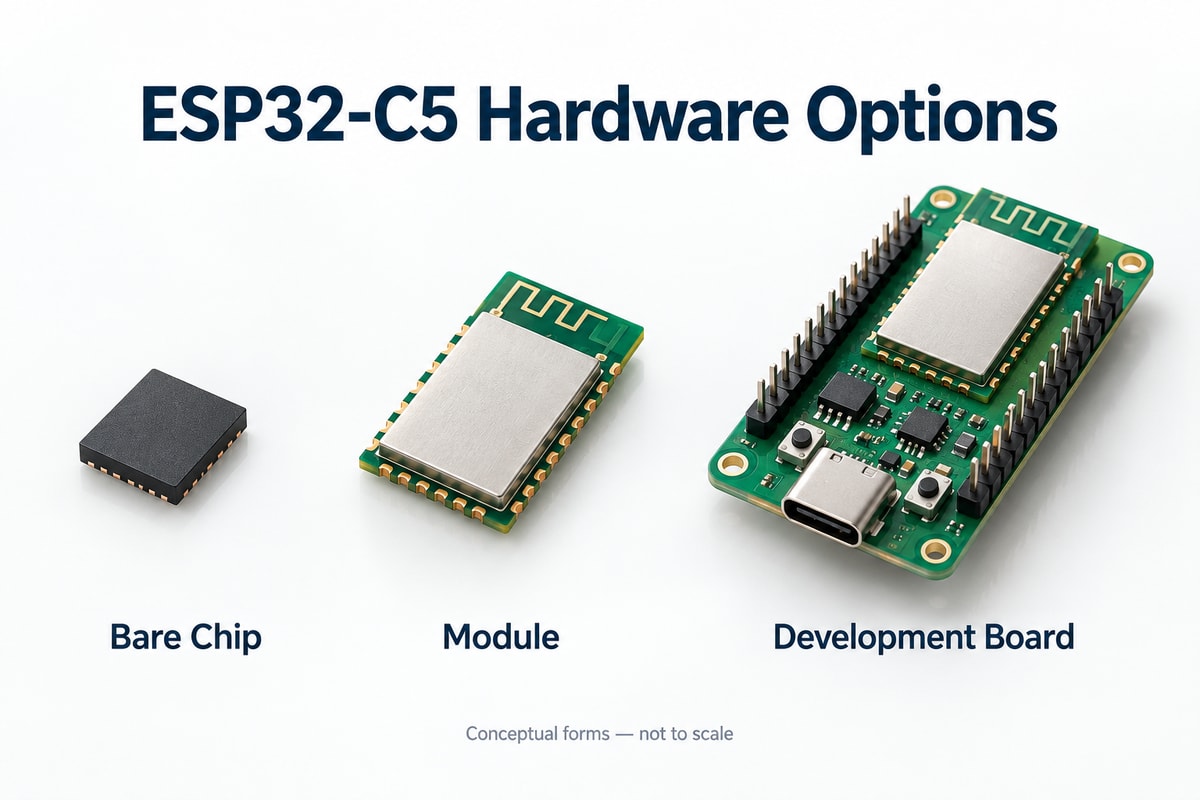
ESP32 Form Factors: C3 vs S3 Chips, Modules and Development Boards

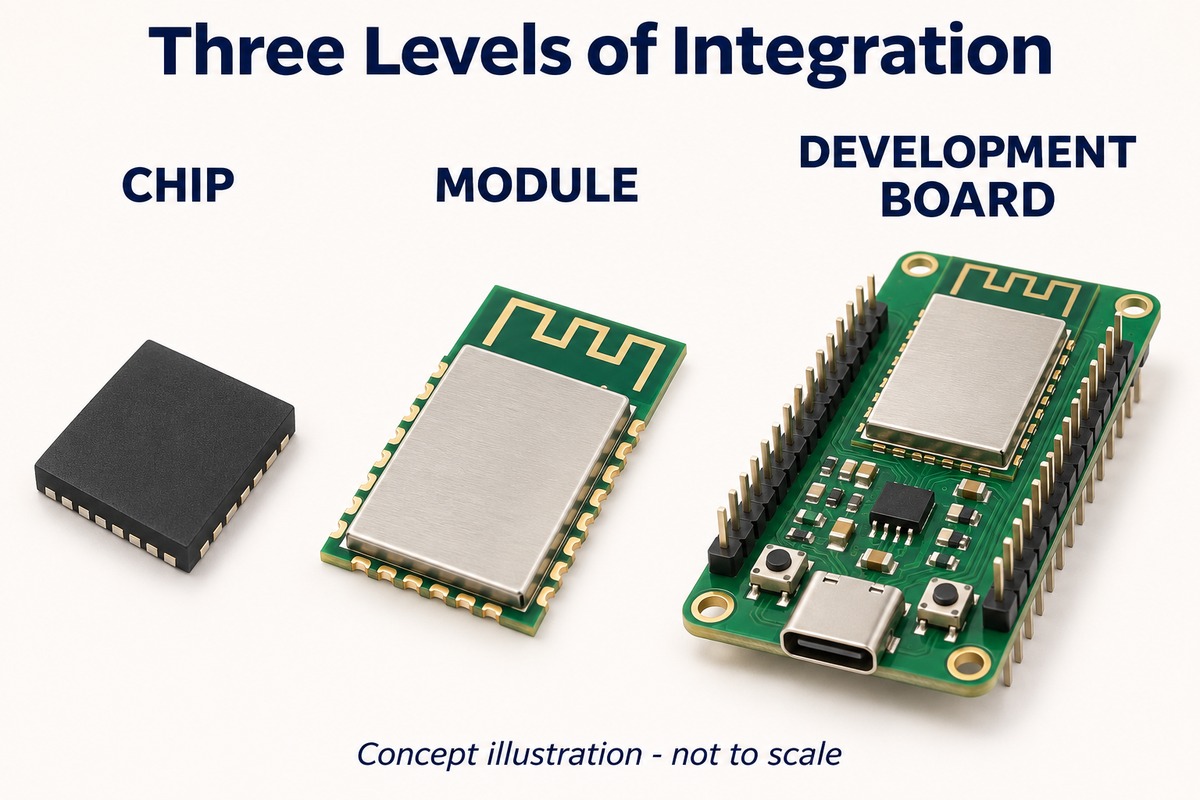
The three forms differ in how much supporting circuitry they integrate. That changes the space occupied by the complete solution and the work remaining on the host PCB.

  • Bare chip — the most integration work remains on the PCB. The surrounding circuit supplies the required power, clock, memory and RF implementation for the selected variant. It offers placement flexibility, but a small QFN package does not mean the complete circuit occupies only that area.
  • Wireless module — more of the circuit comes in a defined footprint. Depending on the model, it integrates memory and an onboard antenna or external antenna connection. The host board still needs suitable power and the specified antenna clearance.
  • Development board — additional hardware supports evaluation. Connectors, headers, regulators and programming circuitry make firmware and peripheral testing convenient. They also add size and power consumption that may be unnecessary in a custom product.

For enclosure planning, the antenna keepout is part of the installation space even where it contains no components. Nearby copper, metal hardware or batteries can affect the onboard antenna, so the module outline alone does not describe all the space it needs.

ESP32 C3 vs S3

ESP32 Module Selection for PCB Assembly

The complete module part number connects the component list to the actual assembly requirements. Modules with similar names or appearances can differ in memory, antenna connection, pin usage and land pattern. A substitution can affect both the physical build and firmware behavior.

The manufacturing implications fall into three areas.

  1. Solder attachment. The land pattern and stencil apertures control where solder paste reaches the module pads. An underside ground pad, where present, also has soldering requirements that must be reflected in the assembly process.
  2. Module handling and reflow. Storage, moisture handling and the reflow profile follow the selected module’s requirements. A physically compatible replacement does not automatically carry identical processing requirements.
  3. Programming and test access. A connection accessible on the prototype may be covered after a display, shield or enclosure is fitted. Accessible power, ground, reset and programming signals support fixture-based programming and testing at the appropriate assembly stage.

At EBest Circuit, our PCB fabrication, component sourcing and assembly services bring the selected module into the complete board build. Matching PCB data and the specified component list establish what is assembled; firmware-loading and functional-test requirements define what the completed board must demonstrate.
FAQs About ESP32 C3 vs S3

Can an ESP32-C3 replace an ESP32-S3 without changing the PCB?

Generally, no. The chip packages and pin assignments differ, and modules are not interchangeable simply because they belong to the ESP32 family. A replacement also needs compatible peripherals, memory and firmware.

Can the same firmware binary run on both chips?

No. The C3 uses RISC-V and the S3 uses Xtensa, so the firmware must be built for the correct target. Some application source code can be reused, but pin assignments, drivers and target-specific features still need adaptation.

Do ESP32-C3 and ESP32-S3 support Bluetooth Classic audio?

Neither supports Bluetooth Classic. A conventional Bluetooth A2DP speaker application cannot be implemented simply by selecting one of these chips for its Bluetooth LE capability.

Does an ESP32 S3 USB C port always provide USB OTG?

No. USB-C describes the connector. The board’s wiring, controller selection, power circuit and firmware determine whether the port supports native USB device or host operation.

Is ESP32-C6 a direct upgrade from both C3 and S3?

It is a different option rather than a universal replacement. Its Wi-Fi 6 and IEEE 802.15.4 capabilities address different connectivity needs, while the S3 remains relevant for applications needing its processing, memory and display or camera resources.

Can both chips be programmed with the Arduino IDE?

Yes. The Arduino-ESP32 platform supports both families. Selecting the correct board target is essential, and a library that assumes a particular processor, pin map or peripheral may need changes when moving between them.

For your ESP32 C3 vs S3 project, match the processor to the workload and the exact module to the finished board. Discuss PCB fabrication, component sourcing and assembly with EBest Circuit at sales@bestpcbs.com.

You may also like

ESP32-C5: Specs, Dual-Band Wi-Fi 6, and PCB Assembly

October 30th, 2026

ESP32-C5 is a wireless microcontroller that brings 2.4 GHz and 5 GHz Wi-Fi 6 to connected products. For engineering teams, its appeal is the ability to use either Wi-Fi band while retaining a compact embedded platform. For production, the important distinction is whether the product uses the bare chip, a ready-made module, or a development board during evaluation—each leads to different purchasing, fabrication, and assembly requirements.

At EBest Circuit (Best Technology), we bring PCB manufacturing, component sourcing, and assembly together for custom electronics. For an ESP32-C5 product, that means building from your released hardware files and agreeing on inspection and functional testing before production. Send your board files, BOM, and intended quantities to sales@bestpcbs.com for a project-specific quotation.

ESP32-C5

ESP32 C5 Features: Key Specifications for Product Selection

ESP32 C5 features combine a RISC-V processor, dual-band wireless connectivity, and interfaces for sensors and control electronics. The following specifications describe the chip family; module ordering codes and development-board versions determine the actual memory and accessible connections in a purchased product.

Specification ESP32-C5 capability
Main processor Single-core 32-bit RISC-V, up to 240 MHz
On-chip ROM 320 KB
High-performance SRAM 384 KB
Low-power SRAM 16 KB
Wi-Fi 2.4 GHz and 5 GHz; Wi-Fi 6 / IEEE 802.11ax
Other wireless connectivity Bluetooth LE and IEEE 802.15.4 for Thread and Zigbee
Chip-level GPIO count 29; usable connections depend on package, memory configuration, and integration
Example peripheral interfaces SPI, UART, I2C, I2S, SDIO slave, USB Serial/JTAG, and CAN FD
Package options QFN48 or LGA48, 6 × 6 mm; part-number dependent
Flash and PSRAM Configuration depends on the chip or module ordering code

Memory capacity needs a complete part number. Flash stores firmware and persistent data; PSRAM provides additional working memory. Neither is interchangeable with the on-chip SRAM figures above. A BOM entry containing only “ESP32-C5” leaves the memory configuration and package unresolved.

ESP32 WiFi 6: What Does the C5 Add at 5GHz?

The C5 adds 5 GHz access to an ESP32 WiFi 6 product, providing an alternative when 2.4 GHz is congested. The improvement depends on the access point, signal strength, interference, and application traffic—not the band name alone.

  • Band selection: A nearby access point with a cleaner 5 GHz channel may improve connectivity; 2.4 GHz can be more useful across distance and obstacles. Evaluate both with the intended enclosure, antenna orientation, and mounting surface.
  • OFDMA and Target Wake Time: Wi-Fi 6 can organize traffic among compatible devices and support scheduled wake periods. Benefits depend on network support and configuration, so these features do not guarantee lower latency or power consumption in every installation.
  • Connection limits: Dual-band capability does not mean two simultaneous independent Wi-Fi links or 5G cellular service. Firmware must support the intended access-point configuration and channels permitted in the operating region.

ESP32 C5 vs C6: Which Fits Your Connectivity Requirements?

The clearest difference in ESP32 C5 vs C6 selection is 5 GHz Wi-Fi support. Both provide Wi-Fi 6, so “Wi-Fi 6 required” alone does not establish a need for C5.

Comparison ESP32-C5 ESP32-C6
Wi-Fi bands 2.4 GHz and 5 GHz 2.4 GHz
Main CPU RISC-V, up to 240 MHz RISC-V, up to 160 MHz
Bluetooth LE Supported Supported
IEEE 802.15.4 Supported Supported
Thread and Zigbee Supported with the appropriate software Supported with the appropriate software
Strong reason to evaluate Products that need access to 5 GHz Wi-Fi Products whose wireless requirements are satisfied by 2.4 GHz Wi-Fi and/or 802.15.4

Selection beyond Wi-Fi: Choose C5 when deployment networks require 5 GHz or testing demonstrates its value; C6 remains relevant when 2.4 GHz meets the requirement. CPU clock alone does not predict performance—workload, memory, software, and network activity also matter.

Migration requirements: Review hardware and firmware when moving from C6 to C5. Similar family names do not establish pin-compatible replacement.

ESP32-C5 Module or Bare Chip: What Changes with ESP32-C5-WROOM-1?

The main difference is how much wireless circuitry arrives as part of the purchased component. A bare chip leaves more integration on the custom PCB; a WROOM module packages the SoC, memory configuration, and supporting circuitry, but still needs a suitable host board and power supply.

Hardware choice Antenna arrangement What changes for production
ESP32-C5 bare chip Defined by the customer's RF implementation Manufacture the released RF geometry and clock circuitry; assemble the chip and supporting components
ESP32-C5-WROOM-1 Onboard PCB antenna Use the module land pattern and preserve specified antenna clearances
ESP32-C5-WROOM-1U External-antenna connection Include the antenna, cable, mounting position, and connection operation in the assembly package

GPIO and footprint selection: The WROOM family exposes up to 22 GPIOs, compared with 29 at chip level. Module pads, chip-package pins, and development-board headers are different references; the schematic symbol, footprint, and BOM must match the selected hardware.

An external antenna changes mechanical integration, not just the BOM. Neither antenna option eliminates the need to validate performance inside the finished enclosure.

ESP32-C5

ESP32-C5-DevKitC-1: What Can You Validate Before Building a Custom PCB?

ESP32-C5-DevKitC-1 lets you validate firmware, wireless behavior, and peripheral interfaces before releasing custom hardware. It combines a WROOM module with power circuitry, programming connections, buttons, and headers; those development-board features are not all included in the module itself.

  • Network and firmware behavior: Test the intended access points, recovery after disconnection, application data transfer, and firmware updates. Record the settings and firmware version so the custom board can repeat the same checks.
  • Peripheral operation: Exercise attached sensors and interfaces under realistic operating conditions. This establishes a useful reference when troubleshooting the first custom assembly.
  • Power measurements: Regulator losses, LEDs, and the USB interface can contribute to board current. Measure the relevant supply rail rather than treating USB-input current as module consumption.

Repeat the relevant tests on the custom board and inside its enclosure. Changes to the supply, connectors, and antenna surroundings can affect behavior even with unchanged firmware.

ESP32 C5 Projects: Which Product Applications Benefit from Dual-Band Wi-Fi?

The strongest ESP32 C5 projects use dual-band connectivity to meet a deployment requirement. Connected appliances, indoor monitoring, building controls, and industrial communication interfaces are useful candidates when their networks and installation conditions justify 5 GHz support.

  • Connected appliances: Support either Wi-Fi band available at the installation. Setup and reconnection behavior matter as much as initial connectivity.
  • Indoor monitoring: Transfer logs or frequent measurements over a cleaner 5 GHz channel near an access point, where testing confirms an advantage.
  • Building controls: Combine local sensing and control with Wi-Fi, Thread, or Zigbee. The software architecture determines how the device participates in the wider system.
  • Industrial communication interfaces: Transfer local equipment data to a wireless network. The complete product still needs the appropriate isolation, protection, and physical-layer components.

A low-duty-cycle sensor with reliable 2.4 GHz coverage may gain little from 5 GHz. Coverage and antenna installation can outweigh Wi-Fi generation, particularly with distant access points or metal enclosures.

What PCB Materials and Manufacturing Controls Do ESP32-C5 Products Need?

ESP32-C5 boards need consistent reproduction of the approved stackup, copper geometry, and assembly features. Material selection follows the design's dielectric, thermal, and fabrication requirements; 5 GHz operation alone neither requires a specialty RF laminate nor justifies an arbitrary FR4 substitution.

  • Layer count and stackup: Espressif recommends four layers in its chip-level layout guidance. A completed module's carrier board may have different requirements; agree the four-layer PCB stackup or other validated construction before fabrication.
  • 50 Ω RF transmission lines: Where the board carries an RF feed line, use the specified characteristic impedance and approved stackup. Trace width depends on dielectric thickness and material properties, so a width copied from another board is insufficient.
  • Antenna clearances and CAM control: Preserve copper keepouts, ground structures, solder-mask openings, and board-edge relationships. Panel supports or CAM copper additions must not encroach on released antenna regions; proposed changes require engineering approval.
  • Finish, pads, and vias: Match the specified surface finish, pad geometry, and via treatment to the assembly process. Exposed ground pads and nearby vias need particular attention to prevent uncontrolled solder loss.

These controls reproduce the customer's validated hardware; they do not replace RF or antenna development.

How Do You Prepare an ESP32-C5 Board for PCB Assembly and Production Testing?

Prepare one consistent hardware revision, a complete purchasing specification, and a repeatable acceptance test. The ordered chip or module must match the BOM, footprint, and manufacturing files.

Production input Required detail
PCB fabrication package Gerber and drill files, fabrication requirements, and approved revision
Assembly and procurement package BOM with manufacturer part numbers, placement data, assembly drawings, relevant schematic, quantities, supplied parts, and explicit do-not-populate positions
Programming and test package Firmware files, programming instructions, test connections, equipment requirements, and pass/fail limits

Package-specific assembly controls: Stencil apertures, paste deposition, placement, and reflow must suit the actual package and BOM. Follow component storage, moisture-handling, and thermal requirements rather than applying a generic reflow profile.

Inspection versus functional testing: SPI checks paste deposits, AOI examines visible assembly features, and X-ray can inspect concealed joints where appropriate. These PCBA inspection and testing methods complement functional testing; they do not prove wireless performance.

For a repeatable C5 functional test, define:

  1. Power-up checks and firmware identification.
  2. Connection and data transfer on each required Wi-Fi band, using a defined access point and configuration.
  3. Operation of fitted interfaces, with a consistent fixture arrangement and acceptance limits.

Agree customer firmware, test equipment, and the required inspection scope with the assembler before finalizing the production quotation.

ESP32-C5

ESP32-C5 Case Study: From Prototype to PCB Assembly

An EBest Circuit RF-interface order combined PCB fabrication, component sourcing, and SMT assembly for 20 boards. It provides the manufacturing basis for the ESP32-C5 wireless communication terminal discussed here; the C5 application is an adaptation, not an identified feature of the original order.

The terminal uses an ESP32-C5-WROOM-1 to collect local equipment data and send it over 2.4 GHz or 5 GHz Wi-Fi. Its carrier accommodates the power input and equipment connections. The recorded customer requirements included production-file approval and individual-board delivery after SMT.

PCB parameter Actual order specification
Construction 4 layers; FR4, Tg130
Finished thickness 1.60 mm ±10%
Copper weight, L1–L4 1 / 0.5 / 0.5 / 1 oz
Surface finish ENIG, specified gold thickness 1 µin
Mask and legend Green solder mask; white silkscreen
  • Fabrication-to-SMT handoff: Our recorded scope included panelization and component procurement. The SMT order referenced the same PCB revision, connecting the bare-board specification with assembly and purchasing requirements.
  • Customer release control: Production-file approval was required before fabrication. This gave the customer a defined review point for the manufacturing data rather than relying on a prototype description.
  • C5 antenna integration: For the terminal adaptation, panel supports and nearby components must preserve the module's antenna clearance. The recorded stackup is a manufacturing reference; the carrier and enclosure need C5-specific validation.
  • Inspection and test preparation: The C5 build requires module and power-circuit solder-joint inspection, programming, startup, interface checks, and data transfer on both required bands. Customer firmware, access-point settings, and pass/fail limits define the functional test.

The commercial value is a coordinated fabrication, sourcing, and SMT package with a controlled board revision. For the C5 terminal, adding the approved assembly and test instructions establishes a practical handoff for pilot and repeat builds.

Why Choose BestPCBS for ESP32-C5 PCB Manufacturing and Assembly?

BestPCBS combines PCB fabrication, sourcing, and assembly through EBest Circuit (Best Technology). Our PCB assembly service supports custom C5 hardware from a released manufacturing package through inspection and agreed testing.

  • SMT and mixed assembly: SMT and through-hole processes accommodate modules, compact supporting components, and wired connectors on the same product.
  • DFM and assembly review: We review fabrication data, stackup requirements, and assembly inputs to identify manufacturing issues before production.
  • Component sourcing: Full turnkey, partial turnkey, and consignment options let you choose which parts we procure. Manufacturer and authorized-distributor sourcing supports BOM control.
  • SPI, AOI, and X-ray: Our equipment includes 3D solder paste inspection, 3D AOI, and X-ray inspection for relevant joint types. Inspection scope follows the assembly's risks and acceptance requirements.
  • Functional test support: We coordinate testing around your firmware, connections, and acceptance limits, connecting assembly checks with product operation.
  • Quality management: ISO 9001:2015 is among our listed quality certifications. Project-specific documentation and acceptance requirements belong in the agreed production scope.

FAQs About ESP32-C5

These questions cover purchasing, software compatibility, and hardware details that affect a C5 production build. Use the exact hardware version when checking compatibility or estimating cost and power.

What Affects the ESP32-C5 Price in a Production BOM?

The exact chip or module, memory configuration, antenna version, order quantity, and sourcing conditions affect component price. A development-board retail price is not a production module price. Compare quotations using the same ordering code, and separate component cost from PCB fabrication, assembly, programming, and test costs.

What Should You Check for ESP32-C5 Arduino Compatibility?

ESP32-C5 is listed as supported in the current Arduino-ESP32 stable and development support tables. Use a release that supports C5 and the appropriate board configuration. Peripheral libraries, flash settings, PSRAM settings, and upload behavior still need application-level testing; support for the SoC does not guarantee compatibility with every library written for another ESP32 device.

Where Should You Check the ESP32 C5 Pinout for Your Exact Hardware?

Use the chip datasheet for package pins, the selected module datasheet for module pads, and the development-board schematic and header table for board connections. Match the hardware revision. A classic ESP32-WROOM or generic 30-pin diagram should not be used as a C5 pin reference.

How Should You Evaluate ESP32 Power Consumption for a C5 Battery-Powered Product?

Measure the complete product through its actual operating cycle, including wake-up, sensing, network connection, transmission, and sleep. Battery life depends on the time spent in each state, regulator losses, and peripheral loads. A chip sleep-current figure alone does not represent the average current of a finished product.

Does the ESP32-C5 TWAI Controller Need an External CAN Transceiver?

Yes. Connection to a physical CAN bus requires an external transceiver. The controller handles protocol functions; the transceiver provides the bus interface. Match the transceiver, protection circuitry, termination, and firmware configuration to the required bus implementation, including CAN FD where applicable.

Does Using ESP32-C5-WROOM-1U Remove the Need for Final-Product RF Validation?

No. The external antenna, cable, enclosure, and mounting arrangement can affect wireless performance. Validate the finished assembly in the intended configuration and operating environment. Replacing an antenna or changing its mounting position can require renewed evaluation.

Bring your ESP32-C5 manufacturing package to EBest Circuit for a quotation covering PCB fabrication, component sourcing, assembly, and the agreed testing scope. Email the files, quantities, and target delivery date to sales@bestpcbs.com so we can assess the build around your actual hardware configuration.

You may also like

1k Resistor Color Code, Testing and PCB Selection

October 24th, 2026

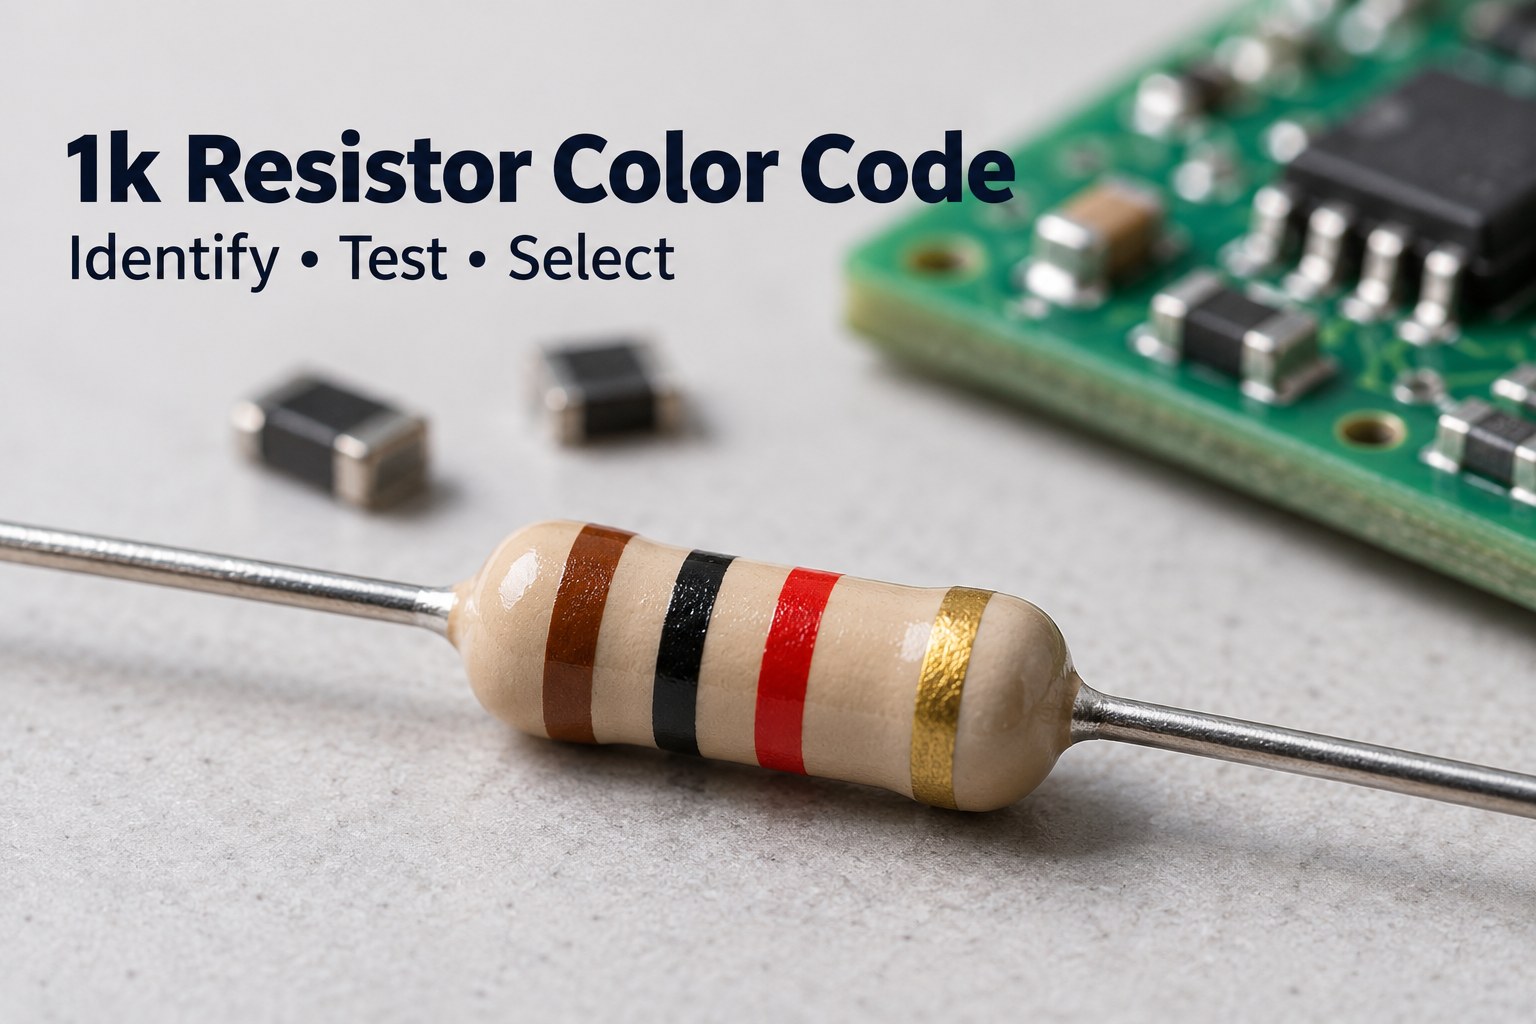
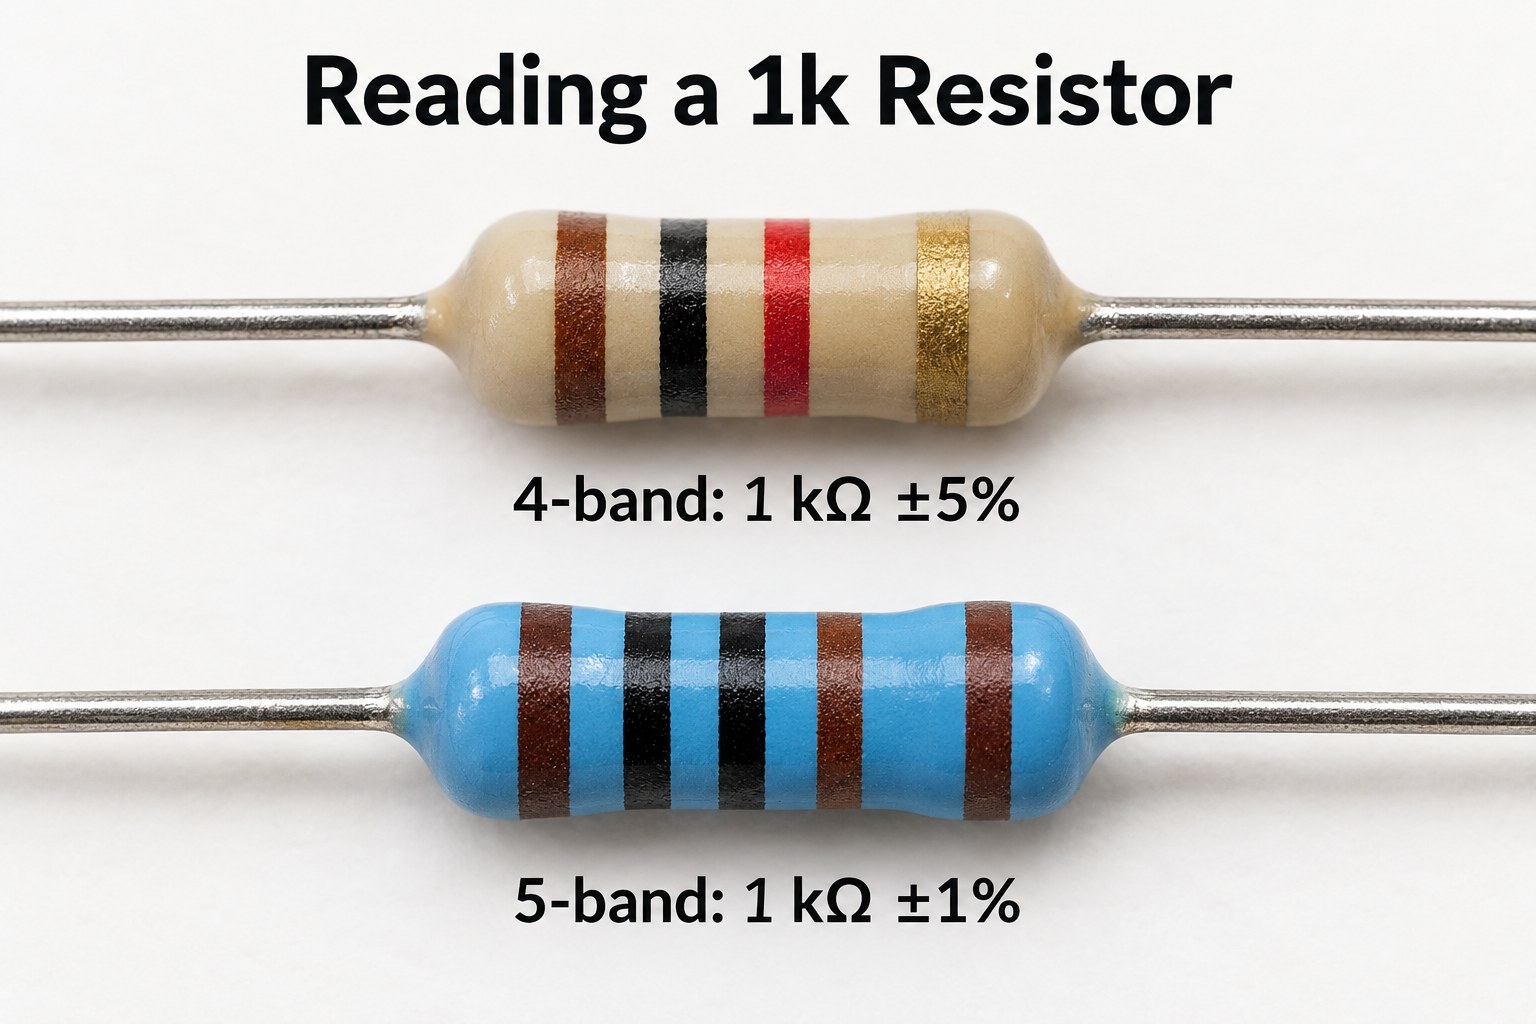
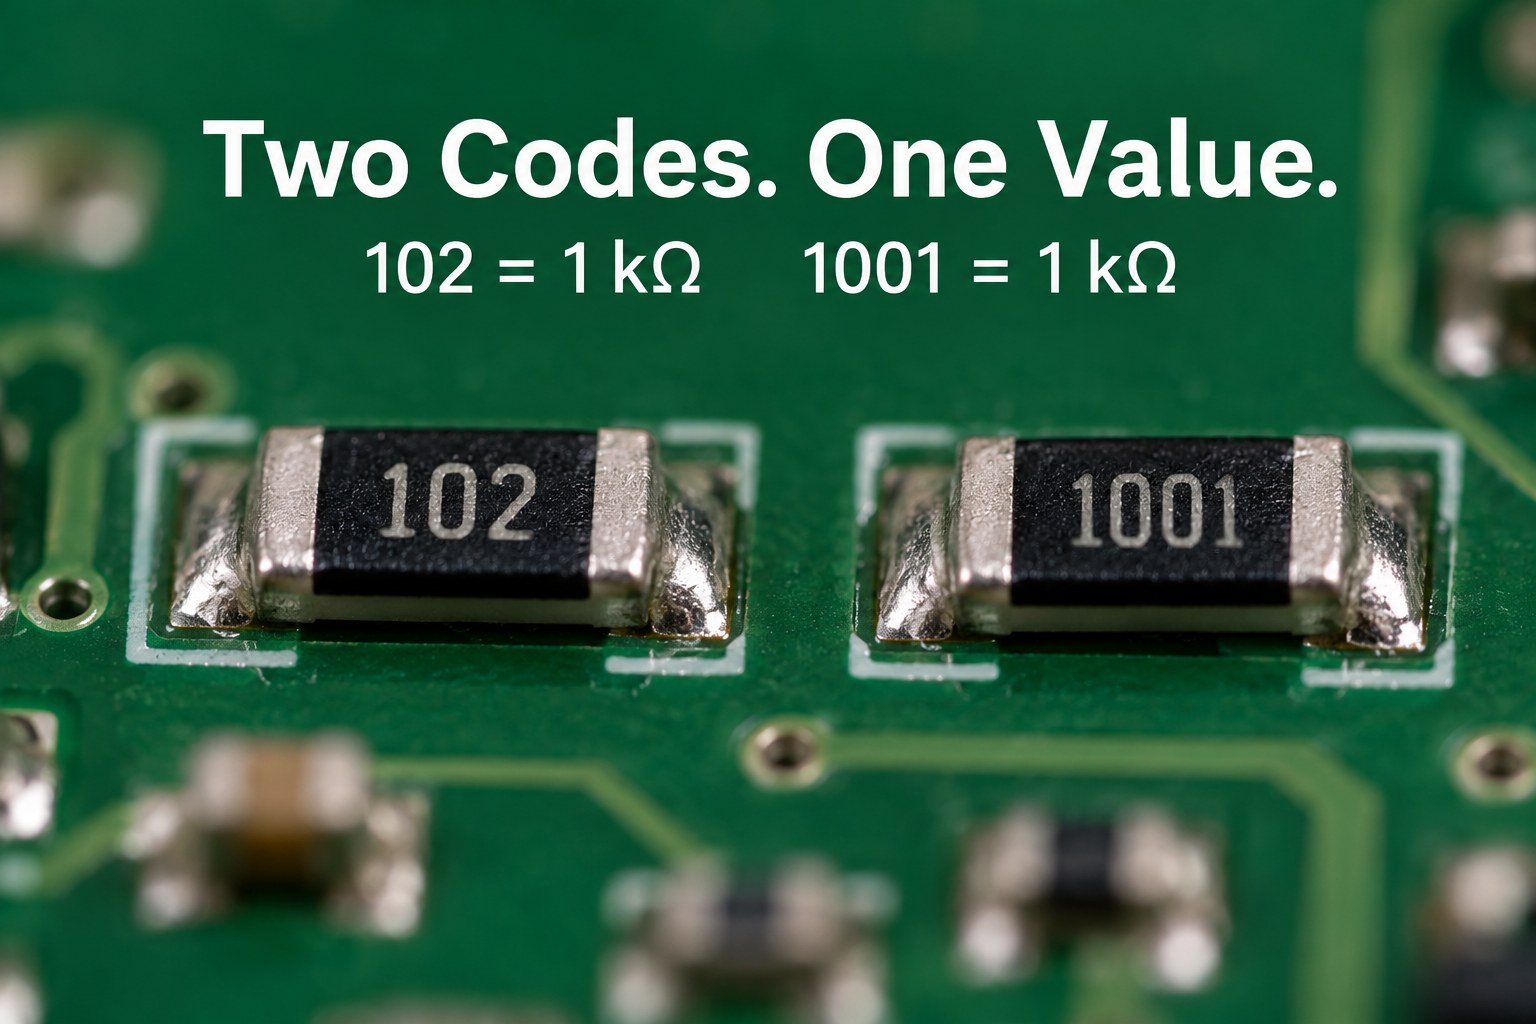
The 1k resistor color code is brown–black–red–gold for a common four-band resistor with ±5% tolerance. A five-band version with ±1% tolerance uses brown–black–black–brown–brown. Both represent 1,000 Ω, also written as 1 kΩ or 1k0. Surface-mount versions may carry the marking 102 or 1001, while smaller packages may be unmarked. Once you identify the value, check tolerance, power rating, and package before using the resistor in a circuit.
At EBest Circuit, we support component sourcing, PCB fabrication, and assembly. Send your BOM, Gerber files, and assembly requirements to sales@bestpcbs.com for a quotation, including manufacturer part numbers and approved resistor alternatives where available.

1k resistor color code with brown black red gold bands

Key Takeaways

  • A 1k resistor has a nominal resistance of 1,000 Ω; 1 kΩ, 1k0, and 1000 Ω describe the same value.
  • Brown–black–red–gold identifies a four-band 1 kΩ resistor with ±5% tolerance, corresponding to 950–1,050 Ω under its specified reference conditions.
  • Brown–black–black–brown–brown identifies a five-band 1 kΩ resistor with ±1% tolerance, corresponding to 990–1,010 Ω.
  • In conventional SMD resistance coding, 102 and 1001 both represent 1 kΩ; the marking alone does not establish power rating.
  • With 5 V directly across a 1 kΩ resistor, current is 5 mA and power dissipation is 25 mW.
  • A resistance measurement should be taken with power removed and stored charge discharged; parallel circuit paths can make an installed resistor read below its individual value.
  • A 1 kΩ resistor can serve as an LED current limiter, pull-up, pull-down, or part of an RC network when the circuit calculations support that choice.
  • A suitable replacement must match resistance and meet the required tolerance, power, voltage, temperature, and footprint specifications.

What is a 1k ohm resistor?

The letter k means kilo, or one thousand, so a 1k resistor has a nominal resistance of 1,000 ohms. It belongs to a family of fixed-value components used to control current and establish voltage or timing relationships.

You may see the value written as 1 kΩ, 1k, 1K, 1k0, or 1000 Ω. In component-value notation, a letter can replace the decimal point: 1k0 means 1.0 kΩ, while 1k5 means 1.5 kΩ.

Keep the component value separate from its PCB reference designator. A label such as R12 identifies the resistor’s position in the circuit. The schematic or BOM supplies its resistance and other specifications.

Resistance also differs from power rating. A 1 kΩ, 0.125 W chip resistor and a 1 kΩ, 1 W leaded resistor have the same nominal resistance, but their permissible operating conditions differ. Selecting a part starts with the resistance value and continues with its electrical and mechanical ratings.

What color is 1k?

For a four-band resistor, the first two bands provide the significant digits, the third gives the multiplier, and the fourth indicates tolerance.

For brown–black–red–gold, brown represents 1, black represents 0, and red means multiply by 100:

10 × 100 = 1,000 Ω

The gold band specifies ±5% tolerance. A different final band changes the tolerance while the first three bands continue to indicate 1 kΩ.

The 1k resistor color code 5 band sequence follows the same digit-and-multiplier principle. Five-band resistors use three significant digits followed by a multiplier and tolerance band. Brown–black–black gives 100; the next brown band multiplies that by 10.

Four-band and five-band 1k resistor color codes
Band format Color sequence Resistance calculation Tolerance Initial resistance range
Four-band Brown–black–red–gold 10 × 100 ±5% 950–1,050 Ω
Four-band Brown–black–red–brown 10 × 100 ±1% 990–1,010 Ω
Four-band Brown–black–red–red 10 × 100 ±2% 980–1,020 Ω
Four-band Brown–black–red–silver 10 × 100 ±10% 900–1,100 Ω
Five-band Brown–black–black–brown–brown 100 × 10 ±1% 990–1,010 Ω
Five-band Brown–black–black–brown–red 100 × 10 ±2% 980–1,020 Ω

These ranges describe initial tolerance under the specified reference conditions. Operating temperature and long-term drift are separate considerations.

Read the bands with the tolerance band at the end; its spacing often helps establish direction. Body color is not a dependable resistance identifier. For faded or heat-damaged markings, confirm the value against documentation and an isolated measurement.

What Are the SMD Codes for a 1k Resistor?

The common three-digit SMD code for 1 kΩ is 102. The first two digits form 10, and the final digit specifies a multiplier of 10²:

102 → 10 × 10² = 1,000 Ω

The four-digit equivalent is 1001:

1001 → 100 × 10¹ = 1,000 Ω

Distinguishing these codes from similar markings prevents a tenfold value error during inspection or rework.

SMD resistor markings 102 and 1001 representing 1 kilohm
SMD marking Conventional interpretation Resistance
101 10 × 10¹ Ω 100 Ω
102 10 × 10² Ω 1 kΩ
103 10 × 10³ Ω 10 kΩ
1000 100 × 10⁰ Ω 100 Ω
1001 100 × 10¹ Ω 1 kΩ
1002 100 × 10² Ω 10 kΩ

A four-digit code of 1000 represents 100 Ω, not 1,000 Ω. Interpret the full marking system rather than reading the printed digits as an ordinary number.

Small chip resistors may have no readable marking. For these components, use the reel label, manufacturer part number, BOM, and placement records. A top-side photograph alone may be insufficient to distinguish several values in the same package.

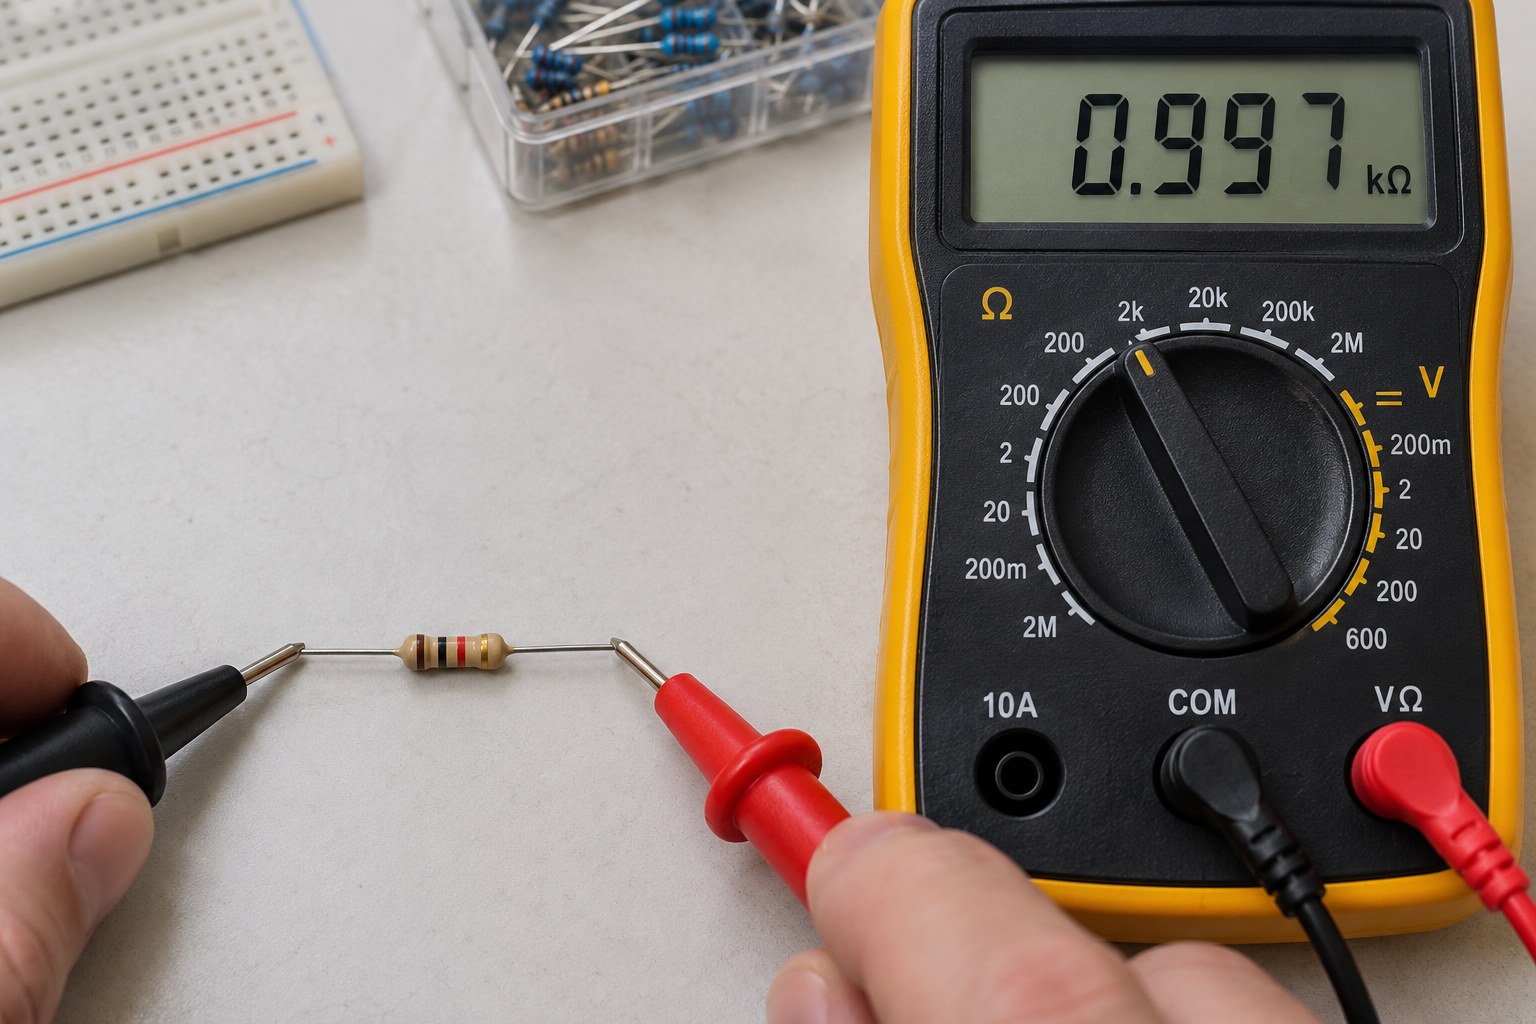
How Do You Test a 1k Resistor with a Multimeter?

Use resistance mode and measure the component with the circuit unpowered. For a dependable component-level result, isolate the resistor from other conductive paths.

Illustration of isolated resistor measurement showing 0.997 kilohms
  1. Remove circuit power. Disconnect batteries, external supplies, and other sources that could energize the board.
  2. Discharge stored energy. Use an appropriate discharge method and verify that residual voltage has fallen before measuring resistance.
  3. Select the resistance function. Use autoranging or a manual range that includes 1 kΩ.
  4. Check probe contact. Touch clean terminals or pads and allow the reading to settle.
  5. Isolate the component if necessary. Lift one lead or remove the resistor when the surrounding circuit affects the measurement.
  6. Compare the result with its tolerance. Include the meter’s accuracy when judging a reading close to a limit.

For example, 997 Ω is within the initial range of a 1 kΩ ±1% resistor. A reading of 1,030 Ω fits a ±5% part but falls outside the initial ±1% range, assuming suitable measurement conditions and sufficient meter accuracy.

An installed resistor can read lower because the meter sees parallel paths. Two 1 kΩ resistors connected in parallel produce an equivalent resistance of 500 Ω. That reading says something about the network between the probes, rather than proving either resistor is faulty.

If a reading remains unstable, inspect probe contact, residual charge, and semiconductor paths before replacing the component. Document the measured value and test conditions when the result will be used for a production or repair decision.

How Much Current and Power Does a 1k Resistor Carry?

Current depends on the voltage across the resistor, while heating depends on the power dissipated in it.

Use:

I = V ÷ R

P = V² ÷ R = I² × R

For a nominal 1,000 Ω resistor, the following values apply when the stated DC voltage appears directly across its terminals.

Voltage across resistor Calculated current Calculated dissipation Selection implication
3.3 V 3.3 mA 10.89 mW Usually modest thermal loading; verify the selected part
5 V 5 mA 25 mW Compare with allowable power at operating temperature
9 V 9 mA 81 mW A 0.1 W part would operate at 81% of its nominal rating before derating
12 V 12 mA 144 mW Exceeds a 0.125 W nominal rating
24 V 24 mA 576 mW Exceeds a 0.5 W nominal rating

These calculations use nominal resistance. At a fixed voltage, the lowest resistance within tolerance produces the highest current and dissipation.

For a 1 kΩ ±5% resistor with 12 V across it:

Pmax = 12² ÷ 950 ≈ 0.152 W

Include supply tolerance as well when establishing the worst operating case.

A useful power-based current calculation is:

I = √(Pallowable ÷ R)

For 1 kΩ and 0.25 W, this gives approximately 15.8 mA. It is a power-based boundary under the assumed conditions, rather than a recommended operating point. The selected part’s temperature derating, voltage limit, pulse capability, and mounting conditions still apply.

How Do You Choose the Power Rating and Package?

Choose the power rating from the highest expected dissipation and the allowable dissipation at the actual operating temperature. Then select a package that fits the PCB and can meet those conditions.

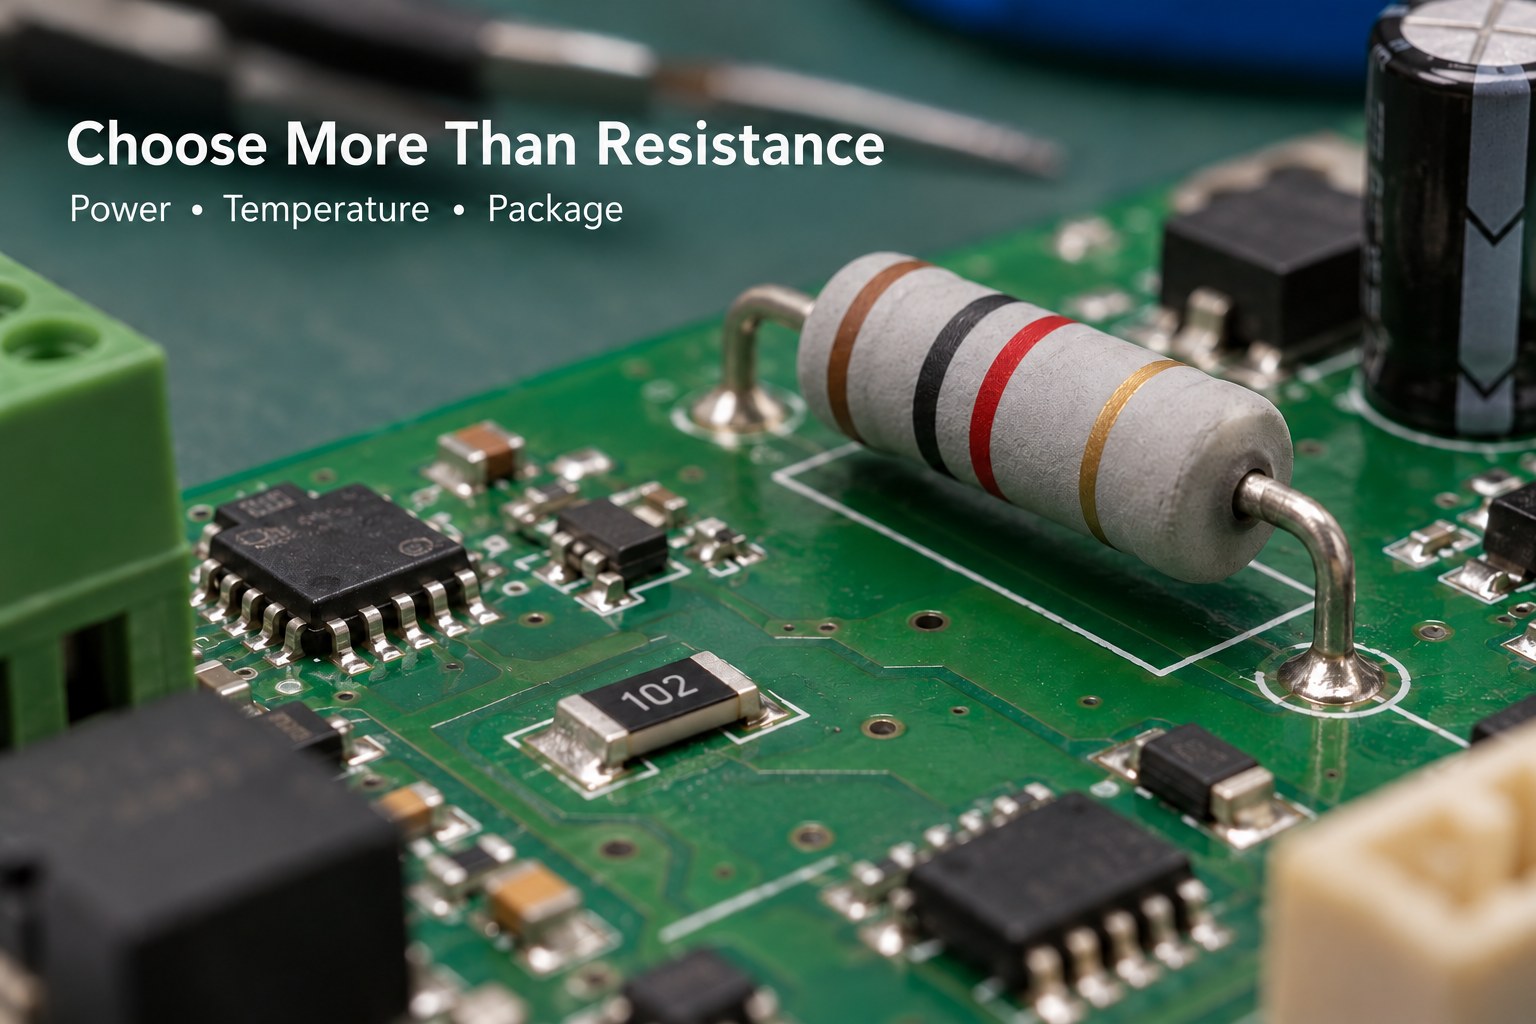
Package size does not establish a universal wattage. Resistor families with the same body dimensions can have different ratings, termination designs, and mounting requirements.

Axial and surface-mount 1k resistors for power and package selection
Specification What to define Why it matters
Resistance 1 kΩ nominal Establishes the intended circuit behavior
Initial tolerance For example, ±1% or ±5% Sets the initial resistance spread
Rated power Series-specific rating and reference temperature Establishes the starting thermal limit
Temperature derating Allowable power at the expected local temperature Accounts for reduced cooling margin
Working voltage Continuous voltage across the resistor Adds a limit separate from power
Pulse capability Pulse amplitude, duration, repetition, and waveform Supports startup and transient evaluation
Temperature coefficient Required ppm/°C range Controls resistance change with temperature
Package and footprint Imperial/metric size, pads, or lead spacing Ensures mechanical and assembly compatibility
Resistor technology Thick film, thin film, metal film, or another suitable type Affects stability, noise, and pulse behavior
Procurement details Manufacturer part number and approved alternatives Keeps repeat builds consistent

For reference, the standard-power ratings in Vishay’s D/CRCW e3 family include 0.10 W for 0603, 0.125 W for 0805, and 0.25 W for 1206 under the datasheet conditions. These are specific product-family examples, not ratings that apply to every resistor in those sizes.

Consider a hypothetical 0.25 W resistor whose datasheet specifies linear derating from full power at 70°C to zero at 155°C. At 100°C, its allowable power would be:

0.25 × (155 − 100) ÷ (155 − 70) ≈ 0.162 W

The earlier 12 V example dissipates 0.144 W nominally, leaving limited margin under those assumed conditions. A larger rating or a different circuit arrangement may provide a more suitable operating point.

What is a 1k ohm resistor used for?

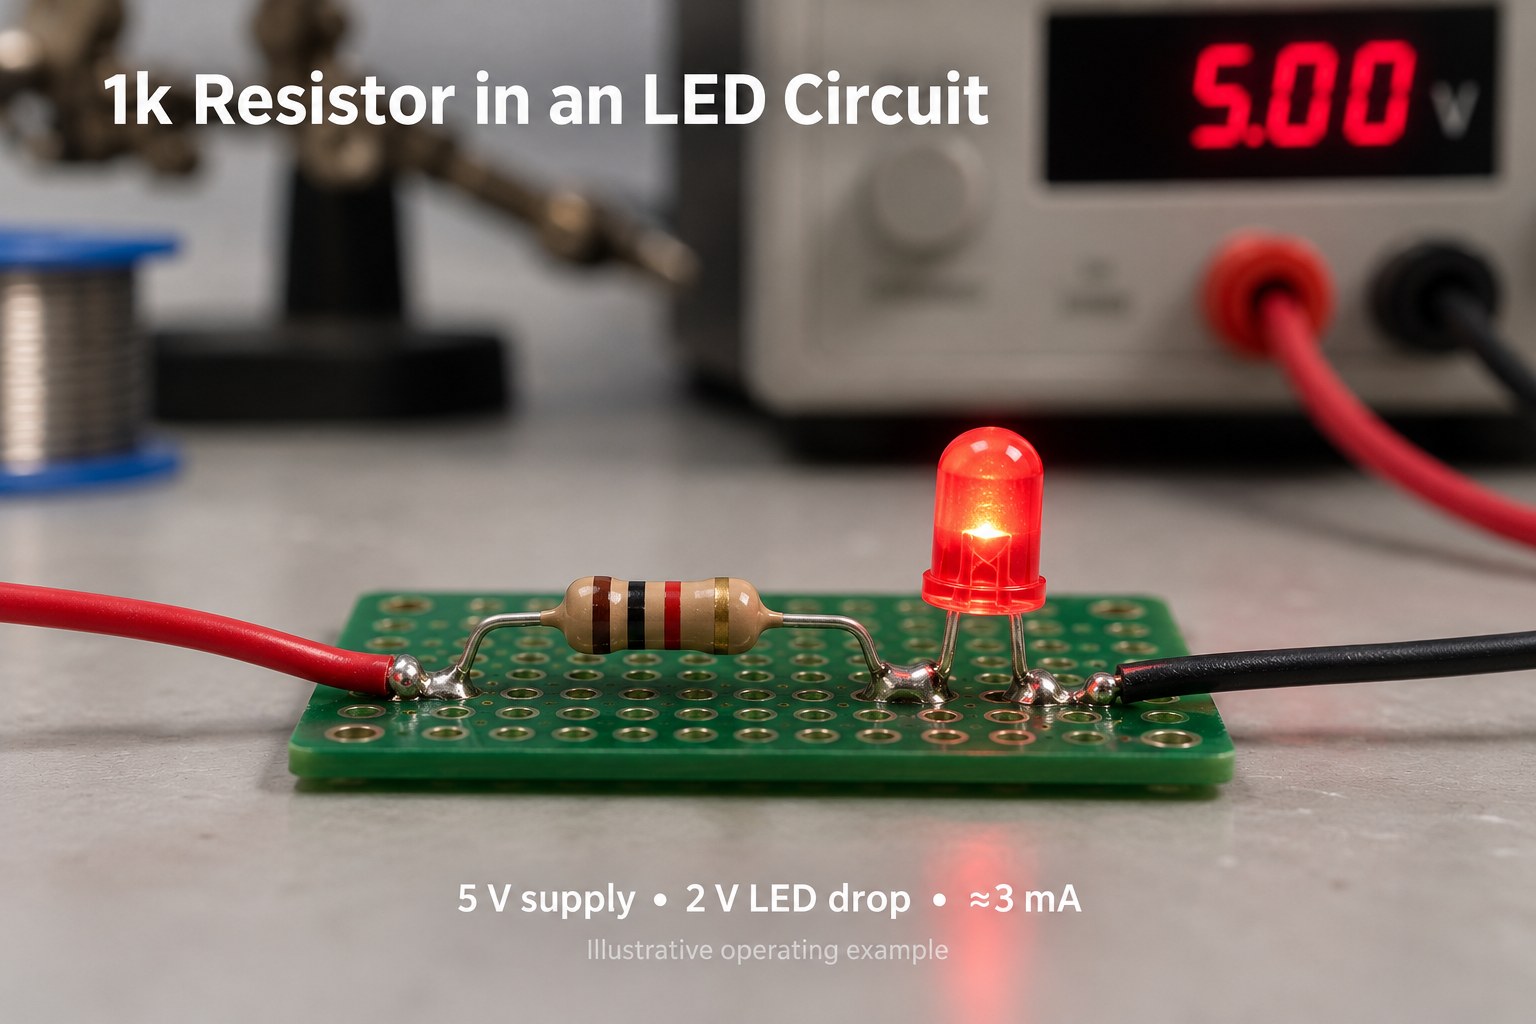
A 1 kΩ resistor can limit current through an indicator LED when its calculated current meets the brightness requirement and remains within the component ratings.

For a simple series circuit:

ILED = (Vsupply − VF − Vdriver) ÷ R

Here, VF is the LED’s forward voltage and Vdriver is any relevant voltage drop in the driving transistor or output stage.

Illustrative 5 volt LED circuit with a 1k current limiting resistor

With an assumed 5 V supply, 2 V LED forward voltage, and negligible driver drop:

ILED = (5 − 2) ÷ 1,000 = 3 mA

The resistor sees 3 V, so its dissipation is:

PR = 3² ÷ 1,000 = 9 mW

This illustrates why the supply voltage should not automatically be used as the resistor voltage. Part of the supply appears across the LED.

For a second example, a 12 V supply and a 2 V LED forward voltage produce approximately 10 mA and 0.10 W in the resistor. Compare that dissipation with the selected resistor’s derated rating.

Check maximum supply voltage, minimum LED forward voltage, resistor tolerance, and the driver’s current capability when calculating the highest current. For minimum brightness, evaluate the opposite limits and the LED’s specified light output.

When Is a 1k Pull-Up or Pull-Down Resistor Suitable?

A 1 kΩ pull-up or pull-down provides a relatively strong bias compared with 10 kΩ. It can establish a logic state with less sensitivity to leakage current, while drawing more current when an output drives against it.

For a 3.3 V pull-up connected to an output held near ground:

I ≈ 3.3 ÷ 1,000 = 3.3 mA

The driving pin must support that current while maintaining a valid logic-low voltage. Account for any additional pull-ups already connected to the same net.

On an open-drain bus, resistance also affects rise time. A lower pull-up resistance charges bus capacitance faster, but increases the low-state current requirement. TI’s I²C guidance calculates a lower resistance limit from output sink capability and an upper limit from rise time and bus capacitance.

For a simple RC rise measured from 30% to 70% of the supply:

tr ≈ 0.8473 × R × C

With 1 kΩ and 100 pF, the calculated rise time is approximately 84.7 ns. Use the actual interface requirements and connected-device specifications to judge suitability.

For a static input or battery-powered circuit, a higher resistance may provide adequate bias with lower current consumption. Select the value from leakage, noise exposure, timing, and power requirements.

How Do Tolerance and Temperature Affect Circuit Accuracy?

Tolerance describes the initial resistance range. Temperature coefficient describes how resistance changes with temperature, commonly expressed in parts per million per degree Celsius.

Using a simplified linear estimate:

ΔR = R × TCR × ΔT

For a 1 kΩ resistor with a temperature coefficient magnitude of 100 ppm/°C over a 50°C change:

|ΔR| ≈ 1,000 × 100 × 10⁻⁶ × 50 = 5 Ω

That is approximately 0.5% of nominal resistance. Initial tolerance, self-heating, and long-term drift are separate contributors to the total error budget.

In a voltage divider, the resistance ratio determines the unloaded output. Two nominal 1 kΩ resistors across 5 V produce 2.5 V at their midpoint.

If both resistors are ±1%, opposing tolerance extremes give:

Vout,min = 5 × 990 ÷ (1,010 + 990) = 2.475 V

Vout,max = 5 × 1,010 ÷ (990 + 1,010) = 2.525 V

Loading adds another source of error. A 10 kΩ load connected from the midpoint to ground is in parallel with the lower 1 kΩ resistor. Their equivalent resistance is approximately 909 Ω, reducing the nominal output to about 2.381 V.

For an RC network, a 1 kΩ resistor and 100 nF capacitor give a nominal time constant of 100 µs. Both component tolerances influence the result, so choose their specifications together.

Can You Replace a 1k Resistor with Another Value?

A different resistance is suitable only when the resulting circuit behavior remains acceptable. A change that works in an indicator circuit may alter an analog gain, timing interval, or protection function beyond its intended range.

For a temporary equivalent resistance:

  • Two 500 Ω resistors in series produce 1 kΩ.
  • Two 2 kΩ resistors in parallel produce 1 kΩ.
  • A 680 Ω resistor and a 330 Ω resistor in series produce 1,010 Ω, which is 1% above 1 kΩ before component tolerances are included.

Evaluate power in each resistor separately. With two equal 2 kΩ resistors in parallel, each sees the full applied voltage and ideally dissipates half the total power. Actual ratings and thermal coupling determine whether the arrangement is suitable.

For a production replacement, retain the required resistance and review tolerance, power, working voltage, temperature coefficient, pulse behavior, and footprint. A higher wattage part can be useful if its dimensions and other properties fit the design.

At EBest Circuit, providing approved manufacturer part numbers and alternatives helps us coordinate sourcing with the assembly BOM. Identify any resistor positions with critical accuracy or pulse requirements so those limits remain visible during substitution review.

FAQs About 1k Resistors

Q1: Does a 1k resistor have polarity?

A1: A standard two-terminal fixed resistor is nonpolarized and can function electrically in either orientation.

Q2: Should a good 1k resistor make a continuity tester beep?

A2: Many meters have a continuity threshold well below 1 kΩ, so use resistance mode and read the displayed value.

Q3: Does the sixth band on a resistor add another resistance digit?

A3: In a common six-band system, the sixth band indicates temperature coefficient; confirm the marking convention for the selected series.

Q4: Can a 1k resistor replace a fuse?

A4: A standard resistor does not provide a fuse’s specified interruption behavior; use the protection component required by the circuit design.

Q5: Does a blue resistor body always mean 1% tolerance?

A5: Body color varies between products, so establish tolerance from the bands, part number, or datasheet.

Q6: Can a resistor pass a resistance test and still fail during operation?

A6: Yes, a low-power resistance measurement may miss faults that appear under heat, voltage stress, or mechanical movement.

Q7: Is a 1k resistor suitable for every transistor base connection?

A7: The appropriate base resistance depends on drive voltage, required collector current, switching conditions, and the transistor’s specified behavior.

How Can EBest Circuit Support Your PCB Assembly?

At EBest Circuit, we support PCB fabrication, component sourcing, and assembly for prototypes and production builds. Share your component requirements early so we can review BOM completeness, resistor footprints, sourcing options, and the inspection or testing needed for your board.

For a quotation, send your Gerber files, BOM, pick-and-place file, assembly drawings, quantities, and test requirements to sales@bestpcbs.com. Include approved alternatives and any critical resistance tolerance, power, temperature, or pulse requirements to help us prepare the build accurately.

You may also like

How Is Component Lead Forming Done Before PCB Assembly?

October 23rd, 2026

Component lead forming bends and trims a component's terminals to fit the PCB footprint without transferring damaging loads into the package. A usable form has more than the right spacing: it also needs the correct bend location, radius, body clearance and lead length. For through-hole assemblies, we need the exact component part number and assembly drawing to resolve those dimensions before insertion, rather than forcing a mismatched component into the board.

Component lead forming with preformed axial resistors and a forming jig; AI illustration

What Is Component Lead Forming?

Electronic component lead forming is the controlled preparation of lead geometry before assembly. It can produce a simple right-angle bend, a specified offset or an approved stand-off shape. Trimming controls lead length; forming controls the path and position of the lead. They are related operations, but one does not automatically establish the requirements for the other.

The component body is not a handle for bending its leads. A part may still fit the holes after rough handling while its lead-to-body interface has been damaged. Fit, package condition and electrical performance therefore answer different acceptance questions. An acceptable shape also has to survive handling between the forming station and PCB insertion.

Which Dimensions Should a Lead Forming Drawing Specify?

The drawing should define the finished shape using identifiable reference points, not just a distance dialed into a tool. Include the component outline, lead cross-section and tolerances alongside the PCB footprint. A center-to-center pitch and an outside-to-outside measurement are not interchangeable.

Drawing input What needs to be defined What it prevents
Component identity Manufacturer, exact part number, package and drawing revision Applying another package's forming limits
Lead size Round-wire diameter or rectangular-lead width and thickness Selecting a die or hole for the wrong cross-section
Body-to-bend clearance The body reference and the start of the permitted bend Bending into a seal, coating or molded exit
Bend geometry Inside radius, angle, direction and any approved offset A sharp crease or an uncontrolled twist
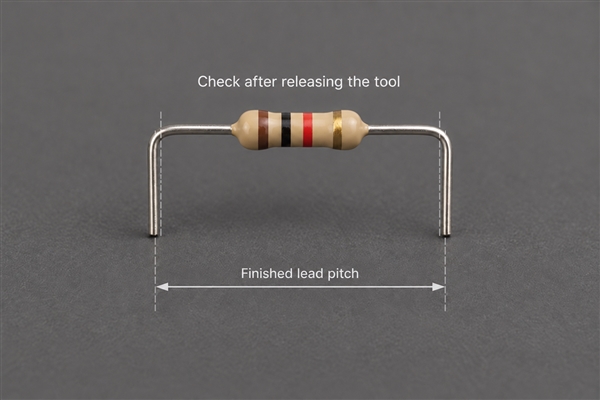
Finished lead pitch Center-to-center spacing, measurement height and tolerance Accepting a tool setting instead of the released part
Body position Orientation, polarity and required stand-off Reversed parts or contact with nearby features
Trimmed length Lead-tip position relative to the board and soldering requirement Insufficient protrusion or interference below the PCB

For a multi-lead package, one total span is insufficient: individual terminal positions must match the footprint. When a supplier changes the package outline or lead dimensions, the previous forming setup needs review even if the electrical description is unchanged.

How Do You Choose the Lead Bend Radius?

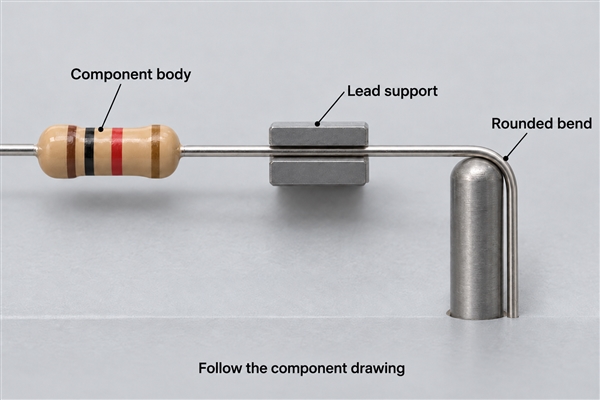
Choose the bend radius from the exact component's approved forming instructions. Lead diameter alone is not enough when package construction, lead material, plating and bend direction differ. A radius measured at the inside of the curve must not be confused with the centerline radius.

For example, onsemi's axial plastic-package guidance AND8390/D specifies a radius no smaller than the lead diameter, limits the angle to 90 degrees and calls for a single forming operation. Its body-to-bend minimum is 1.5 times the typical lead diameter, with at least twice the diameter preferred. These are conditions for the packages covered by that guidance, not a universal rule for resistors, LEDs, capacitors or all transistor packages.

The drawing must also leave enough straight lead for the support tool. If the required footprint forces the bend into a prohibited region, changing the footprint or using an approved preformed component is preferable to tightening the bend until the part fits. Do not resolve a clearance conflict by silently replacing the manufacturer's radius requirement.

How Can You Prevent Stress at the Component Body?

Support the lead between the package and the forming point so that the tool takes the reaction load. Pulling the free end while holding the body allows that load to reach the lead exit. The support must restrain the lead without cutting it, stripping the finish or crushing the package.

Lead support between the component body and rounded bend, shown as an illustrative setup

Glass packages require particular care. For the Vishay SOD-57, SOD-64, DO-35 and DO-41 glass diodes covered by document 86158, the body-to-bending-position distance is greater than 1.5 mm. The specified fixture grips the lead wires and keeps mechanical load off the glass body. This is a package-specific requirement, not permission to grip the glass itself.

That document includes a minimum clamping-force instruction expressed as 2.5 kg. It must be interpreted with the original fixture arrangement and applicable device documentation; it is not a general hand-pliers setting. A controlled setup must distinguish sufficient restraint from excessive lead deformation. Unexpected tool marks or package movement require a setup review, not simply more force.

How Do Axial and Radial Lead Forming Differ?

Axial component lead forming positions leads that leave opposite ends of the body. The finished geometry must accommodate the body length, clearances on both sides and the two bends. An axial component lead former therefore needs space for the actual body and suitable support for both wires, not merely a groove labeled with the target pitch.

Radial lead forming deals with leads leaving the same side of the body. Changing their spacing can load the nearby lead exits, especially when the available straight length is short. Radial component lead forming also needs to preserve polarity, lead order and the component's intended seating height. Do not treat every two-lead radial part as mechanically equivalent to an axial resistor.

Flat transistor leads introduce another issue: bending through the thin dimension is mechanically different from sideways bending across the width. A TO-92 lead forming tool must match the particular pin arrangement and approved bend location. The package name alone does not establish a permitted offset or bending direction.

How Do You Select a Component Lead Forming Tool?

Select a component lead forming tool by lead shape, supported diameter or thickness, bend profile and finished spacing. An electronic component lead former should hold the part consistently without using its body as a reaction stop. Accessibility matters too: the tool must leave room for the required straight section near the package.

Tool approach Useful role Check before use
Fixed or adjustable lead bending and component forming tool Repeatable simple axial bends Groove geometry, body clearance and released pitch
Component lead forming pliers Local offsets or specified lead shapes Jaw profile, contact marks and operator repeatability
Component lead forming machine Repeated parts with controlled feed and setup Package compatibility, tooling condition and first-piece results

A component lead forming kit can help with prototype work, but its available shapes do not override component requirements. The same applies to a lead forming tool for resistors and capacitors: sharing a tool is reasonable only where the two devices' permitted geometry and support conditions actually match.

For larger runs, an electronic component lead forming machine needs a verified setup rather than a copied setting from a different package. A component lead former with multiple stations should maintain the same reference orientation through feeding, forming and cutting. Before releasing a batch, compare the first formed parts with the approved drawing and check that feeding has not reversed the component orientation.

How Should Component Leads Be Trimmed?

Trim to the specified finished length while preventing the cutting action from pulling on the lead-to-body interface. Support and cutting sequence depend on the package and tooling. Keep cut fragments away from parts and PCB assemblies, and inspect the cut end for a burr that could obstruct insertion.

For the glass-diode packages in Vishay document 86158, simultaneous cutting of both leads is not permitted in the illustrated arrangement. Separate cutting steps or a staggered cutting arrangement are shown instead. The document allows simultaneous bending with its specified support conditions. Cutting and bending are therefore not interchangeable when deciding which operations can be performed together.

Where trimming occurs after insertion, support must also protect the board, pads and any existing solder connection. For a through-hole component fitted to a multilayer PCB, use the finished board thickness and seating height to establish the required lead length, not the layer count. The finished protrusion should come from the applicable assembly requirement, not an arbitrary universal length. A shorter lead is not automatically a better assembly if it compromises soldering or inspection access.

How Do You Check Lead Pitch After Forming?

Check pitch after removing the forming load, at the drawing's specified measurement location. Elastic recovery can make the released part differ from the tool's nominal setting. A measurement made while the part is still constrained can hide that difference.

Released axial component with center-to-center finished lead pitch indicated; illustrative geometry

For two equal round leads measured across their outside surfaces, subtract one lead diameter to obtain the center-to-center distance. As a dimensional example, a 10.60 mm outside span with two 0.60 mm leads gives a 10.00 mm center pitch. This calculation assumes parallel leads of equal diameter at that measurement height; it is not a forming tolerance recommendation.

Check lead parallelism and seating height as well as pitch. For our FR4 PCB manufacturing, the drawing's finished-hole size and position must be considered with the actual lead envelope. A nominal drill diameter is not the finished plated-hole diameter. Do not spread or squeeze the component against the board to conceal a mismatch.

What Should You Inspect After Lead Forming?

Inspect the component body, lead exits, bends, finish and final dimensions before accepting the formed parts. Compare with the incoming condition where a mark or crack may already have existed. Appearance alone cannot establish whether a hidden connection or seal remains intact.

Illustrative magnified inspection of a formed lead and component body
Inspection area Look for Follow-up when it does not match the requirement
Body and lead exit Cracks, chipped coating, displacement or a changed lead exit Segregate the part and assess package damage
Bend Creasing, twisting, inconsistent radius or repeated rework Check the profile and support arrangement
Lead surface Deep jaw marks, exposed base metal or damaged finish Compare with the device's permitted tooling marks
Dimensions Pitch, parallelism, angle, length and stand-off Measure in the released state against the drawing
Insertion fit Leads aligned with holes without forced reshaping Review both formed geometry and PCB footprint
Electrical condition Results required by the device and test plan Record failures without treating continuity alone as full qualification

An inspection record is most useful when it identifies the part number, lot, drawing revision, setup, sampled quantity and measured dimensions. A photograph can document a visible condition, but cannot prove a numerical radius or hidden seal integrity by itself. Abnormal parts need disposition before insertion, when access to the lead exits is still clear.

How Can You Keep Lead Forming Consistent Across a Batch?

Use an approved first piece, defined setup controls and checks at meaningful change points. Tool wear, a new component lot or a changed package can alter the output even when the operator uses the same setting. Record the released dimensions rather than treating a machine setting as the acceptance result.

Separate unformed, accepted and held parts so rejected pieces cannot re-enter production. Packaging between operations should protect the formed leads from being compressed or tangled. If a component needs repeated straightening to pass the insertion check, stop and resolve the mismatch rather than cycling the lead through additional bends.

For a new footprint, our PCB prototype manufacturing can provide the actual board for a fit review before the design moves to volume assembly. The useful result is a checked component-and-board combination, not a nominal pitch verified on only one side of that interface.

What Information Do We Need for Through-Hole Assembly?

We need the BOM with exact manufacturer part numbers, PCB fabrication data, assembly drawing, orientation requirements and any approved lead-form dimensions. Include the original component instructions when a bend, stand-off or trimming sequence is critical. State whether parts arrive unformed, factory-preformed or customer-prepared.

At EBest Circuit (Best Technology), our PCB assembly service includes through-hole and mixed assembly, incoming inspection, DFA review, insertion and wave soldering. We support tube, tray and loose-part supply as well as other listed packaging formats. The suitable preparation route depends on the component and build requirements; we do not apply one bend specification to every package.

For component lead forming services within a PCBA project, send the drawing, quantity and required inspection records to sales@bestpcbs.com. We can review those inputs with your assembly requirements before quotation. If the package instructions and footprint conflict, that conflict needs an agreed resolution before production.

Component Lead Forming FAQs

How to Clean and Form Component Leads Before Soldering?

Check incoming finish condition before forming. Use only a cleaning method compatible with the component, plating and approved process; abrasive removal of finish or an unapproved chemical treatment can create a solderability problem. Suspect corrosion requires assessment rather than polishing the part until it looks clean. Confirm acceptable surface condition before releasing the part for forming and soldering.

When Shall Sleeving Be Placed on a Component Lead Before Forming?

Where the approved assembly requires insulation sleeving and the finished bend would prevent it from sliding into place, fit the sleeve before that bend. Confirm its final position, temperature suitability and clearance from the solder joint. Do not assume every formed lead needs sleeving or trap a sleeve in a tooling contact area.

Can Through-Hole Forming Rules Be Used for SMT Leads?

Not automatically. SMT component lead forming also involves seating-plane and coplanarity requirements, plus the specific package's permitted reshaping method. A through-hole bend or spacing instruction does not establish an acceptable gull-wing lead profile. Use the component's approved surface-mount geometry rather than adapting the axial-wire examples without verification.

Can a 3D-Printed Lead Forming Jig Replace Metal Tooling?

A resistor lead forming tool made by 3D printing may be useful for a checked prototype geometry. It still needs adequate stiffness, smooth contact surfaces and appropriate ESD controls for the parts being handled. Wear or deflection can change the finished dimensions. It should not be treated as a qualified production fixture merely because one component fits.

You may also like

Thick Film Resistor TCR: Values, Temperature Drift and Selection

October 21st, 2026

Thick film resistor TCR describes how much a resistor’s resistance changes with temperature, usually expressed in ppm/°C. Understanding common TCR ratings helps you estimate temperature drift and its effect on circuit accuracy. Practical examples show when standard thick film resistors meet your needs and when a lower-TCR option is worth choosing.

At EBest Circuit, we’ve supported PCB and PCBA projects for customers in the United States, Germany, and Israel, including established medical device brands. Our dedicated engineering and quality management teams help customers turn design requirements into production-ready boards, with practical support when manufacturing challenges arise.

thick film resistor TCR
Thick film chip resistors in carrier tape before PCB assembly.

What Does Thick Film Resistor TCR Mean?

The temperature coefficient of resistance (TCR) describes the relative change in resistance per degree of temperature change. A value of 100 ppm/°C corresponds to approximately 0.01% per °C.

A positive TCR means resistance increases as temperature rises; a negative TCR means it decreases. A datasheet rating of ±100 ppm/°C specifies a limit under the stated test conditions. It does not mean that every resistor has an actual coefficient of +100 or −100 ppm/°C.

TCR and resistance tolerance describe different sources of error. Tolerance specifies the initial resistance range at a reference condition, while TCR describes temperature-related change. A resistor with tight initial tolerance can still drift noticeably during operation.

What TCR Values Do Thick Film Resistors Offer?

Thick film resistor TCR ratings commonly include ±100 and ±200 ppm/°C, while precision series offer options such as ±50 or ±25 ppm/°C. The available rating depends on the specific series, resistance value, package, and temperature range.

TCR rating Approximate resistance change over 60°C Selection context
±200 ppm/°C ±1.20% General-purpose circuits with a relatively wide error allowance
±100 ppm/°C ±0.60% General-purpose designs requiring less thermal drift
±50 ppm/°C ±0.30% Tighter temperature-stability requirements
±25 ppm/°C ±0.15% Precision applications where this drift fits the error budget

These figures estimate the temperature contribution alone, assuming the stated coefficient applies across the temperature interval. They exclude initial tolerance and long-term resistance change.

Check the TCR specification for the exact orderable part. A series may specify different limits for different resistance ranges, and low-resistance or very high-resistance values may have wider limits. Also check whether the datasheet specifies separate behavior above and below the reference temperature.

How Do You Calculate Resistance Change from TCR?

Multiply the reference resistance by TCR and the temperature change to estimate resistance drift. For an approximately constant coefficient:

ΔR ≈ Rref × α × ΔT × 10⁻⁶

Here, Rref is resistance at the reference temperature, α is TCR in ppm/°C, and ΔT is the resistor’s temperature change in °C. The corresponding percentage change is:

Resistance change (%) ≈ α × ΔT ÷ 10,000

For a 10 kΩ resistor warming from 25°C to 85°C, ΔT is 60°C:

TCR magnitude used Estimated resistance change Change relative to 10 kΩ Estimated resistance range*
25 ppm/°C ±15 Ω ±0.15% 9,985–10,015 Ω
50 ppm/°C ±30 Ω ±0.30% 9,970–10,030 Ω
100 ppm/°C ±60 Ω ±0.60% 9,940–10,060 Ω
200 ppm/°C ±120 Ω ±1.20% 9,880–10,120 Ω

Assumes exactly 10 kΩ at 25°C and an applicable ±TCR limit. Initial tolerance, aging, and other effects are excluded.

A ±100 ppm/°C part therefore contributes approximately ±0.6% temperature-related resistance change over this interval. If its initial tolerance is ±1%, a conservative first-order estimate allows roughly ±1.6% combined deviation before other errors are included.

How Do Self-Heating and PCB Temperature Affect Resistance?

TCR calculations should use the resistor’s operating temperature, not simply the surrounding air temperature. That temperature reflects both heat from the PCB and nearby components and heat generated by the resistor itself.

Resistor power dissipation is P = I²R, or P = V²/R. The resulting temperature rise depends on the package, copper layout, mounting conditions, and airflow; it cannot be determined from power alone.

For example, suppose the local ambient temperature is 60°C, but self-heating raises the resistor to 85°C. Relative to a 25°C reference, a 100 ppm/°C coefficient gives approximately 0.6% resistance change, rather than the 0.35% estimated from ambient temperature alone.

Operating below the power rating does not guarantee negligible thermal drift. For precision circuits, evaluate temperature under the intended load and PCB conditions, while observing the manufacturer’s power-derating limits.

thick film resistor TCR
Concept illustration: heat leaves the resistor through the surrounding air and PCB.

How Does TCR Affect Voltage Dividers and Analog Circuits?

A voltage divider’s temperature stability depends primarily on how its two resistors change relative to each other. Equal fractional changes cancel in the divider ratio, while unequal changes shift the output.

For an unloaded divider with upper resistor R1 and lower resistor R2:

Vout = Vin × R2 ÷ (R1 + R2)

The following example assumes initially equal resistors, a stable input voltage, and the same 60°C temperature rise for both resistors. The listed TCRs represent their actual coefficients in this simplified model.

R1 actual TCR R2 actual TCR R1 change R2 change Output change relative to its initial value
+100 ppm/°C +100 ppm/°C +0.6% +0.6% 0%
+100 ppm/°C −100 ppm/°C +0.6% −0.6% −0.6%
−100 ppm/°C +100 ppm/°C −0.6% +0.6% +0.6%

Two resistors carrying the same ±100 ppm/°C rating are not guaranteed to track each other. Their actual coefficients may differ. For precision dividers and amplifier gain networks, a specified TCR tracking or ratio-temperature-coefficient limit is more useful than matching individual TCR ratings alone.

Temperature gradients also matter. Even resistors with identical coefficients change by different amounts if one runs hotter. Keep ratio-critical resistors close together and away from uneven heat sources; consider a resistor network with specified tracking when the accuracy requirement justifies it.

thick film resistor TCR
Concept illustration: uneven heating can cause different resistance changes even when TCR values match.

When Is a Lower-TCR Resistor Worth Using?

Use a lower-TCR resistor when predicted thermal drift exceeds the resistance-related error allowed by the circuit. This is especially relevant to precision sensing, reference scaling, amplifier gain setting, and measurement equipment operating across a wide temperature range.

For example, if a resistor is allowed only 0.2% temperature-related change over an 80°C interval:

Maximum TCR magnitude ≈ 0.2 × 10,000 ÷ 80 = 25 ppm/°C

A ±25 ppm/°C resistor uses the entire thermal-drift allowance in this estimate. Select a tighter rating if margin is required. If 0.2% is the total accuracy budget, initial tolerance and other errors must receive part of that budget as well.

Circuit requirement Selection approach Main consideration
Pull-ups, logic biasing, and other tolerant functions Standard thick film is often sufficient Confirm that resistance variation remains within functional limits
Moderate precision with tighter thermal limits Evaluate precision thick film Check the exact resistance value and available TCR grade
Low drift combined with low excess noise Compare suitable thin film series Check TCR, noise, stability, and operating limits
Stable divider ratio or amplifier gain Evaluate a matched resistor network Prioritize specified tracking and similar operating temperatures
Significant pulse or surge exposure Choose a suitably rated series Low TCR alone does not establish pulse capability

Precision thick film and thin film should be compared at the part level. Thin film often offers lower TCR and lower excess noise, while precision thick film may meet the accuracy requirement without changing resistor technology. For ratio-based circuits, improving tracking can provide more value than reducing each resistor’s individual TCR.

FAQs About Thick Film Resistor TCR

Can a room-temperature resistance measurement verify TCR?

No. It checks resistance at one temperature. Verifying TCR requires measurements at controlled temperatures, with sufficient settling time and low enough measurement power to avoid significant self-heating.

Are ppm/°C and ppm/K equivalent for resistor TCR?

Yes. A temperature change of 1°C equals a change of 1 K, so the numerical coefficient is the same.

Does a zero-ohm jumper have a useful TCR specification?

Usually, maximum resistance, current rating, and temperature rise are more useful selection criteria. Follow the jumper’s datasheet rather than treating its nominal zero-ohm value as an ordinary resistor in a TCR calculation.

Does laser trimming guarantee low TCR?

No. Laser trimming adjusts resistance toward a target value. It does not, by itself, guarantee a particular temperature coefficient.

Is a negative TCR a sign of a defective resistor?

No. A negative coefficient is acceptable when it falls within the manufacturer’s specification. Whether it suits the application depends on the circuit’s temperature behavior.

Can two resistors with the same resistance and TCR rating be substituted directly?

Not on those two specifications alone. Also compare tolerance, package, power derating, working voltage, pulse capability, and applicable reliability requirements.

For PCB fabrication and PCBA support for your thick film resistor TCR requirements, contact EBest Circuit at sales@bestpcbs.com with your project requirements. Our engineering and quality teams can help coordinate manufacturing requirements from prototype through production.

You may also like

eMMC Replacement: Chip Compatibility and Boot Problems

October 15th, 2026

eMMC replacement can restore a board with failed storage, but matching the original chip’s capacity is not enough. The new device must fit the board, communicate with the processor and contain the software needed to start the system. A chip can be soldered correctly and still leave the board unable to boot.

For products moving to a new memory component or a revised PCB, EBest Circuit (Best Technology) provides PCB fabrication, component sourcing and PCB assembly. These services bring the component supply and board production stages together. For PCB and PCBA support on your hardware revision, contact sales@bestpcbs.com.

eMMC replacement
Illustrative eMMC replacement scene; package and board details vary by device.

Can eMMC Be Replaced on an Existing Board?

Yes, but a removable module and a soldered chip require different replacement methods. The first distinction is how the eMMC connects to the board.

  • Removable eMMC module. The storage sits on a small board connected through a socket or connector. A compatible module can be exchanged without BGA soldering, although it still needs suitable software.
  • Soldered eMMC chip. The device connects through solder balls underneath its BGA package. Replacement requires controlled removal, footprint preparation and installation. Underfill or damaged PCB pads can make the work more difficult.

An eMMC contains both NAND flash and a controller. Replacing the package changes both components; reballing the original package only renews its solder connections. Reballing therefore cannot repair worn flash memory or a failed internal controller.

Using the same part number reduces hardware differences, but a blank chip will not contain the original system image. A donor chip may contain another device’s settings. Neither is automatically ready to boot the receiving board.

What Makes an eMMC Replacement Compatible?

A compatible replacement must match the board’s physical connections, electrical requirements and host support. The full part number matters more than the capacity label or the name “eMMC 5.1.”

Physical fit

Package dimensions, ball pitch, orientation and signal assignments must suit the PCB footprint. Two chips can look similar while having connections that prevent a direct substitution.

Electrical and interface support

The device supply and I/O voltages must suit the board. The processor and replacement also need a compatible bus width and timing mode. A faster eMMC cannot make an unsupported host or PCB operate at a higher speed.

Boot compatibility

The processor’s startup code and bootloader must be able to initialize the device and load its software. Image layout and boot configuration matter alongside the hardware specifications.

Endurance and operating conditions

Temperature grade and write endurance affect suitability after the board starts working. A data logger that writes continuously places different demands on storage from a device that mainly reads a fixed application. Equal capacity does not guarantee equal write performance or service life.

Can a Higher-Capacity eMMC Replace the Original Chip?

Yes, when the board and software support it—but extra chip capacity does not automatically become usable storage. An upgrade can produce three different outcomes.

  • The board boots and uses the extra space. The replacement is compatible, and the image or setup process creates a suitable partition layout.
  • The board boots but shows the old capacity. Cloning the original image can preserve its smaller partitions. The relevant partition and filesystem then need expansion before the extra space is available.
  • The board does not boot correctly. The firmware or programming tools may assume a particular device size or layout. A revised image or platform support may be needed.

Capacity also needs to be understood by storage area. An eMMC has a user area and separate boot hardware partitions. A larger user area does not prove that the boot areas meet the platform’s requirements.

How Does eMMC Chip Replacement Work?

Chip replacement combines data preparation, BGA rework and software restoration. The sequence below describes the work; the heating profile and programming method remain specific to the board.

  1. Identify the fault and preserve readable data. Power, connection or software faults can resemble storage failure. If the original device remains readable, preserve the required contents before removal. A factory recovery image does not replace a backup of unique device data.
  2. Remove the original package. Support the PCB and use a controlled heating profile suited to the board and component. Nearby parts, moisture sensitivity and underfill affect removal. A hot-air station setting alone does not establish the solder-joint temperature.
  3. Prepare the pads and fit the replacement. Remove residual solder and contamination, address pad damage, then align and reflow the new device. Inspect the assembly for placement and solder-joint defects.
  4. Restore the system software. Program the required image, boot settings and supported device-specific configuration. Depending on the platform, programming occurs before installation or through the board’s recovery interface.
  5. Test operation beyond the first boot. Cold starts, restarts and application reads and writes reveal problems that a single successful startup may miss. Production qualification can also include temperature, workload and power-interruption tests.

There is no universal rework temperature or firmware file for every eMMC board. The component limits, PCB construction and platform recovery procedure determine those details.

eMMC replacement
Illustrative BGA rework setup with a controlled hot-air nozzle and supported PCB.

Why Does a Board Fail to Boot After eMMC Replacement?

Successful soldering does not establish that the board can find and run its boot software. The point where startup stops helps distinguish communication problems from missing contents or security restrictions.

Startup symptom Possible cause
eMMC not detected Power, soldering or interface fault
Detected, but no bootloader Missing boot image or incorrect boot settings
Bootloader runs, OS fails Image, partition or filesystem mismatch
OS runs, protected functions fail Missing provisioning or security mismatch
Startup works intermittently Marginal power, signals or solder connections

These are possible causes, not definitive diagnoses. A serial console or recovery interface can help identify the actual failure stage.

The copied image may not include the boot area

Copying the user area does not automatically copy the separate boot hardware partitions or reproduce the device’s boot configuration. If the processor expects its first-stage software in a boot partition, a correct user-area image alone will not start the board.

Device security may require separate provisioning

Some platforms use Replay Protected Memory Block (RPMB) storage for authenticated data. RPMB is not an ordinary filesystem partition that can be migrated with a normal disk copy. A supported provisioning or recovery procedure may be necessary, and some device-bound security states cannot be transferred through a generic chip swap.

eMMC replacement
Illustrative board-level startup debugging through a serial-console connection.

What Changes When an eMMC Part Reaches End of Life?

A discontinued eMMC part can lead to a component substitution, a software update or a PCB revision. Which change is necessary depends on the replacement device, not simply on the end-of-life notice.

  • Component qualification. A different controller or NAND technology can change write behavior and endurance. A replacement that boots still needs to suit the application’s workload and operating temperature.
  • Software adaptation. The bootloader, image preparation or device provisioning may need adjustment. Hardware compatibility alone does not establish that the existing production image will work.
  • PCB changes. Different connections or power requirements can require a board revision. If these remain compatible, the existing PCB may be retained.

Artila’s May 2025 replacement notice illustrates a software-linked migration. For the affected products, an SLC-to-MLC eMMC change accompanied a Linux kernel update from 5.10.x to 5.15.x. This was specific to those products; it does not mean every replacement requires a kernel update.

For ongoing production, keeping the qualified memory part and software revision together helps avoid loading an old image onto a newly introduced device that requires different support.

FAQs About eMMC Replacement

Will eMMC replacement preserve the original data?

Not automatically. Recovery depends on readable original contents or a usable backup. Encrypted data also requires the appropriate keys. Restoring factory firmware may restore operation without bringing back user files.

Can an eMMC chip be replaced without programming?

A compatible module supplied with the correct software may work without a separate programming step. A blank chip used as boot storage normally needs an image and platform-specific configuration, loaded through recovery software or external programming equipment.

Can eMMC Be Replaced with SSD?

An SSD is not a direct replacement for a soldered eMMC chip. SATA and NVMe SSDs use different interfaces. Moving the operating system to an SSD requires a suitable board connection and firmware boot support; cloning software cannot provide either.

Why does eMMC replacement cost vary?

A module exchange involves less soldering work than a BGA chip replacement. Board access, damaged pads, programming and data recovery can add to the work. The component price alone therefore does not represent the total repair cost.

Has eMMC been discontinued?

An end-of-life notice applies to specified parts, not automatically to the entire eMMC category. Availability depends on the manufacturer and ordering code. The relevant notice is the one covering the component used in the design.

A successful eMMC replacement brings the memory, PCB and boot software into agreement. When the change leads to a revised board or production PCBA, EBest Circuit can support PCB fabrication, component sourcing and assembly. Discuss your board project with sales@bestpcbs.com.

You may also like

DDR4 Replacement: Chip Compatibility and PCB Changes

October 15th, 2026

DDR4 replacement can involve a removable RAM module or a memory chip soldered to a PCB. For an embedded or industrial product, a successful chip replacement must work with the existing memory controller, board connections, and firmware. The same DDR4 label—or even the same package—does not establish compatibility.

EBest Circuit (Best Technology) combines PCB fabrication, component sourcing, and SMT/BGA assembly for electronics manufacturing projects. Whether a memory substitution retains the original PCB or requires a revised board, these services support the resulting prototype and production builds. Discuss your DDR4 replacement project with our team at sales@bestpcbs.com.

DDR4 replacement

DDR4 Chip Replacement vs. RAM Module Replacement

A module replacement changes a complete memory assembly. A chip replacement changes an individual DRAM device. The distinction matters because each replacement must fit a different set of existing connections.

Aspect RAM module Soldered DDR4 chip
Replacement unit Complete DIMM or SO-DIMM Individual DRAM device
Board connection Plug-in socket BGA solder joints
Installation Remove and insert PCB assembly or rework
Physical fit Module format and keying Footprint and ball assignment

A laptop with a removable SO-DIMM accepts a compatible module through its memory socket. The module brings its own chips and PCB layout.

On a board with soldered DRAM, the replacement chip must use the connections already routed on the host PCB. Its data width, addressing, and electrical requirements must also suit the memory controller. This makes chip substitution a device-and-board compatibility issue, rather than simply a change in installed RAM capacity.

DDR4 replacement

Can I Replace DDR4 with DDR5?

DDR5 is not a direct replacement for DDR4 in a DDR4-only design. The difference involves the platform, not just memory speed.

  • Controller support. The processor or memory controller must support DDR5 communication. A DDR4-only controller cannot operate DDR5 through a firmware setting alone.
  • Electrical interface. DDR4 and DDR5 use different supply levels and command/address interfaces. Their initialization and training requirements also differ.
  • Module connection. DDR4 and DDR5 modules have different keying. A DDR5 module does not fit a DDR4 memory socket.

For soldered memory, moving to DDR5 can require a new memory circuit, corresponding firmware, and a different processor or controller. It is a platform migration rather than a substitute-part installation.

When the aim is to retain an existing DDR4 product, a compatible DDR4 device is the relevant alternative.

Are DDR4 Chips with the Same Package Interchangeable?

Matching the package is only one part of compatibility. Two devices can look alike while differing in how they connect, store data, or operate.

Five areas explain the differences that matter.

  1. Footprint and ball assignment

    Package dimensions, ball pitch, and ball locations determine physical fit. The function assigned to each ball determines electrical fit. A package that fits the pads is unsuitable if required signals or supplies connect to the wrong locations.

  2. Density and data width

    Density describes storage capacity; x8 or x16 describes the device's data-interface width. Equal capacity does not mean equal organization. The controller must support the replacement's addressing and data arrangement, and a density change can also affect refresh timing.

  3. Timing at the actual operating speed

    A faster-rated chip may support the board's existing data rate, but the selected operating point must be valid for that part. CAS latency, write latency, and other timing settings must satisfy its specifications. The higher speed printed on the part description does not establish this by itself.

  4. Supply and temperature requirements

    The replacement must operate within the board's supply conditions and the product's temperature range. A matching nominal voltage does not establish suitability for every operating environment.

  5. Functions used by the controller

    The new device must support the memory functions that the platform enables. Matching basic capacity and package specifications does not resolve a mismatch in a required function.

A cross-reference tool can identify candidate devices. It does not establish that a candidate will work in a particular circuit. The important result is compatibility with the existing design, not similarity between abbreviated product descriptions.

When Does a DDR4 Replacement Require PCB Changes?

PCB changes are required when the replacement needs connections or electrical conditions that the existing board cannot provide. A change of brand or part number alone does not require a new layout.

The work generally falls into three situations.

  1. Replace the component; retain the PCB

    A device with compatible connections, organization, and electrical requirements may operate on the original board. The assembly BOM changes, while the PCB layout remains the same. This is the simplest substitution when the design supports it.

  2. Retain the PCB; update the configuration

    The replacement may use the existing connections but require different memory timing or controller settings. The change then includes the boot-time memory configuration. Software can adjust supported settings; it cannot create a missing connection or add unsupported controller capabilities.

  3. Revise the PCB circuit or layout

    A different footprint or ball assignment can require new pads and routing. Changes to device count or data-bus organization can alter how the memory devices connect to the controller. Different power requirements may also require changes to the supply circuit.

When routing changes, the electrical quality of the interface matters as much as connectivity. Trace geometry, reference planes, return paths, and data-to-strobe relationships affect signal behavior. The revised board must follow the relevant controller's DDR layout requirements; there is no universal trace-length rule for all DDR4 designs.

A component substitution and a PCB revision are therefore different manufacturing changes. The first can retain the existing bare board. The second requires fabrication and assembly information that reflects the revised design.

DDR4 replacement

Why Can a DDR4 Replacement Boot but Still Be Unstable?

Booting proves that startup succeeded under the conditions present at that moment. It does not prove reliable operation across the product's full workload and environment.

Three factors explain why problems can appear later.

  • Limited timing or voltage margin

    During initialization, the controller configures and trains the memory interface as supported by the platform. The resulting setting may work but leave little room for variation. This room is the operating margin: a narrow margin makes the interface more sensitive to changing conditions.

  • Memory activity beyond the startup sequence

    Sustained reads and writes exercise more addresses and data patterns than a short boot sequence. Problems may become visible only when an application uses a larger memory region or generates heavier traffic.

  • Changes in temperature and supply conditions

    A board that starts at room temperature may behave differently after warming up or under a different electrical load. Temperature and supply variation can expose weaknesses that were not visible during initial startup.

How to distinguish startup success from stable operation

Repeated startup, tests across the intended memory address range, sustained workloads, and testing within the specified environmental range provide broader evidence. Margin analysis can also help reveal how close the interface is to failure.

An error pattern can guide investigation, but it does not identify the cause on its own. Repeatable errors at particular addresses and intermittent errors across many addresses may require different investigations. Device configuration, board behavior, and assembly condition remain relevant alongside the DRAM itself.

FAQs About DDR4 Replacement

Can I use a DDR4 replacement from a different brand?

Yes, if the specific replacement meets the platform's requirements. For soldered DRAM, that includes device organization, connections, and operating specifications. For modules, the host must support the complete module configuration. Brand alone neither proves nor rules out compatibility.

Can ECC DDR4 replace non-ECC DDR4?

Only where the platform supports that module and configuration. ECC requires processor and motherboard support; installing an ECC module does not automatically add error correction. An unsupported combination may fail to boot or operate without ECC.

Are DDR4 UDIMMs and RDIMMs interchangeable?

They should not be treated as interchangeable. RDIMMs buffer command and address signals through a register; UDIMMs are unbuffered. DDR4 versions can fit the same style of socket, but the platform must support the module type. Registered and unbuffered modules should not be mixed.

Does a failed DDR4 chip mean the whole board must be replaced?

Not necessarily. Component repair may be possible if the fault is isolated and the board is suitable for rework. A reported memory error alone does not establish chip failure. The fault, board condition, replacement availability, and rework feasibility determine the repair options.

Does one discontinued DDR4 part mean all DDR4 is discontinued?

No. A lifecycle notice applies to the products named in that notice. It does not establish the status of every DDR4 device or supplier. An available alternative still needs to be compatible with the original design.

A suitable DDR4 replacement can extend the use of an existing product without automatically requiring a new PCB. For component sourcing, PCB fabrication, and assembly support for your next build, contact EBest Circuit at sales@bestpcbs.com.

You may also like

How Power Electronics Interconnects Affect Performance

October 13th, 2026

Power electronics interconnects affect how much heat a power assembly generates, how it behaves during fast switching, and how its connections age. A cool busbar can still have an overheated terminal. A thick copper path can still produce a switching-voltage spike. Understanding the connection itself helps explain why these problems occur.

EBest Circuit (Best Technology) supports PCB fabrication, component sourcing, SMT and through-hole assembly, inspection, and agreed testing. Coordinating fabrication and assembly helps address board-level details such as solderability and terminal-to-hole fit before they become assembly problems. For PCB and PCBA support around your approved power circuit, contact sales@bestpcbs.com.

power electronics interconnects
PCB, power modules, and copper busbar connections in a conceptual power assembly.

What Are Power Electronics Interconnects?

Power electronics interconnects are the conductive connections that carry current through a power assembly—from the semiconductor die to the PCB, power module terminals, and external conductors.

They exist at three levels within the assembly.

  • Inside the package — Bond wires, ribbons, clips, and conductive die-attach layers connect the semiconductor to its package conductors.
  • On the PCB — Solder joints, copper tracks, planes, and plated holes carry current between components.
  • Between assemblies — Module terminals, connectors, cables, and busbars link the board to the wider power system.

A removable connector is therefore only one type of interconnect. Every joint along the current path matters; adding copper elsewhere cannot eliminate a restrictive connection.

How Do Wire Bonds, Copper Clips, and Die Attach Differ?

Wire bonds and copper clips commonly connect the top of the die; die attach joins its underside to a support. They occupy different positions, so die attach is not a direct replacement for a wire or clip.

StructureConnection formMain performance considerations
Wire bondsWires from die pads to package conductorsWire resistance, inductance, and current sharing
Copper clipsBroad copper connections above the dieConnection resistance and inductance
Die attachBonded layer beneath the dieHeat transfer; current flow when conductive

A short, broad copper clip can reduce resistance and inductance compared with a suitable wire-bonded alternative. The benefit depends on the complete package geometry; some packages use both clips and wires for different terminals.

Die attach has a separate job. Soldered or sintered layers provide a heat path from the die into its support and may also carry current. A good top-side connection cannot compensate for poor heat transfer beneath the die.

How Do PCBs Connect to Power Modules and Busbars?

PCBs connect to power modules and busbars through soldered terminals, press-fit pins, bolted terminals, or mating connectors. Each interface carries current and transfers mechanical forces differently.

InterfaceConnection methodKey assembly consideration
Soldered terminalSolder joins terminal and PCBAdequate heat at the joint
Press-fit terminalPin presses against a plated holeMatched pin, hole, and plating
Bolted terminalFastener clamps conductive surfacesContact pressure and mechanical support
Mating connectorDesigned contacts plug togetherMating limits and contact rating

Large copper terminals can draw heat away during soldering, making joint formation harder. Press-fit connections avoid that soldering step, but require the specified hole construction, insertion tooling, and board support.

Press-fit does not automatically mean pluggable. It describes the terminal’s connection to the PCB. A separate mating interface provides repeated plugging and unplugging.

Busbars often carry bulk current between modules and DC-link capacitors, while PCBs carry control, sensing, and other circuit connections. For dimensional options, see standard copper busbar sizes. Width and thickness help describe a busbar, but do not establish its installed current rating by themselves.

Why Do Power Interconnects Overheat?

A connection can overheat even when the larger conductor beside it stays cool. The hot spot may be a narrow track, a terminal contact, or a joint where resistance concentrates heat.

Three conditions explain much of this behavior.

  • High current magnifies small resistance. Resistive loss follows P = I²R. Doubling current produces four times the heat at the same resistance.
  • A small connection can restrict a large current path. A wide busbar does not remove resistance at its terminal. Adding copper away from that joint may leave the hot spot unresolved.
  • Heat cannot escape fast enough. Limited airflow, a crowded enclosure, and nearby hot components can raise the connection’s temperature even without a change in current.

A small resistance can produce meaningful heat. For illustration, a 0.5 mΩ connection dissipates 5 W at 100 A and 20 W at 200 A. These are calculated losses at constant resistance, not temperature rises or current ratings.

Actual operating temperature depends on both heat generation and heat removal. Copper resistance also rises with temperature, so room-temperature resistance alone may understate operating losses.

power electronics interconnects
A bolted busbar joint carries current across the copper contact interface; contact condition and clamping affect the connection.

How Does Parasitic Inductance Affect Fast Switching?

A low-resistance connection can still create a voltage spike during fast switching. Its inductance generates an additional voltage as current changes, following ΔV = L × di/dt.

For illustration, 20 nH at 500 A/µs contributes 10 V. This is the inductive contribution, not a prediction of the complete switching waveform.

The important geometry is the complete current loop, including its return path. A thick conductor with a distant return path can still form a large loop. Two layout features help explain the difference.

  • Nearby outgoing and return paths reduce loop inductance. Conductor thickness alone does not provide the same effect.
  • A nearby decoupling capacitor can shorten the switching-current loop. Long connections between the capacitor and switching devices add to that loop.

Package terminals and PCB connections contribute as well. Together with circuit capacitance, inductance can produce overshoot and ringing. This is why adding copper thickness may reduce resistive loss without resolving a switching-voltage problem.

power electronics interconnects
Closely coupled outgoing and return conductors reduce the enclosed loop area. An insulating layer keeps the conductors electrically separate.

What Causes Power Interconnects to Fail Over Time?

An initially sound connection can weaken through repeated heating and cooling. Joined materials expand by different amounts, placing cyclic strain on their interfaces.

The damage appears differently depending on the connection.

  • Wire bonds can develop heel cracks or lift at the bond interface. Repeated strain damages the wire or its attachment point.
  • Solder joints can develop fatigue cracks. Cyclic deformation progressively damages the connection.
  • Die-attach layers can deteriorate. Damage beneath the die can impair heat transfer and raise operating temperature.

Pressure-based terminal connections have a different requirement: they must maintain suitable contact through service conditions. Mechanical support and the specified assembly process help preserve that interface.

Thermal cycling and power cycling stress an assembly differently. Thermal cycling changes its temperature through the surroundings. Power cycling heats the semiconductor through electrical operation, often concentrating temperature changes near the die. Passing one test does not automatically establish performance under the other.

A room-temperature resistance measurement describes the connection’s initial condition. Durability depends on how that construction responds to the temperature changes and mechanical stresses it will experience in service.

FAQs About Power Electronics Interconnects

Are power electronics interconnects just connectors?

No. They also include package connections, PCB copper paths, solder joints, busbar interfaces, and die-attach layers that carry current. Connectors are one part of that wider current path.

Can a busbar replace the PCB?

A busbar can carry part of the bulk-current path, but does not normally replace the PCB’s control, sensing, and component-interconnection functions. Many power assemblies use both.

Does press-fit mean the connection is pluggable?

No. Press-fit describes how a terminal engages a plated board hole. Repeated mating requires an interface designed for it. Removing or replacing a press-fit component must follow the applicable product instructions.

Does low resistance mean low inductance?

No. A connection can have low resistance and still form a large current loop. Resistance influences conduction loss; loop inductance influences the additional voltage produced during rapid current changes.

Does high current always mean high voltage?

No. Low-voltage circuits can carry high current and generate substantial resistive heat. Voltage suitability involves separate insulation and spacing requirements. Both must match the application.

For PCB fabrication and assembly supporting power electronics interconnects, EBest Circuit (Best Technology) can review manufacturability and coordinate sourcing, assembly, inspection, and agreed testing. Contact sales@bestpcbs.com to discuss the board-level connections in your power assembly.

You may also like