PCB manufacturing PCB manufacturing
Home > Blog

PCB Assembly

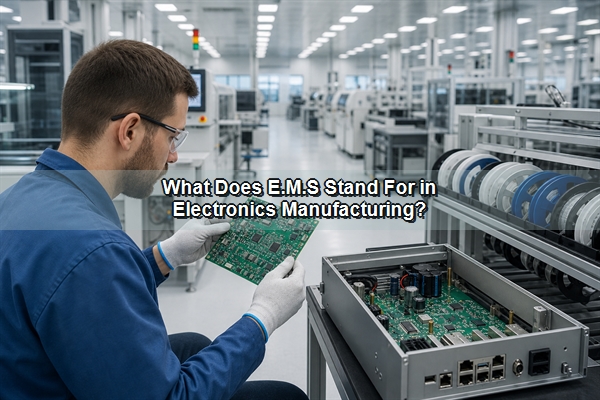
EMS Full Form: How Electronics Go From Design to Delivery
Friday, November 6th, 2026

EMS stands for Electronics Manufacturing Services. In electronics, it means hiring a specialist to perform agreed manufacturing work. That could mean assembling and testing a circuit board, or it could mean sourcing parts, assembling the complete product, testing it in its case, and preparing it for shipment. EMS is the service arrangement, not the name of a single process.

Imagine you have designed a small industrial temperature monitor. You have the circuit files and a list of parts, but you do not have a production line. How do those files become a device with a working sensor, a display and a housing? Follow the example below. It is a teaching scenario, not a real customer project.
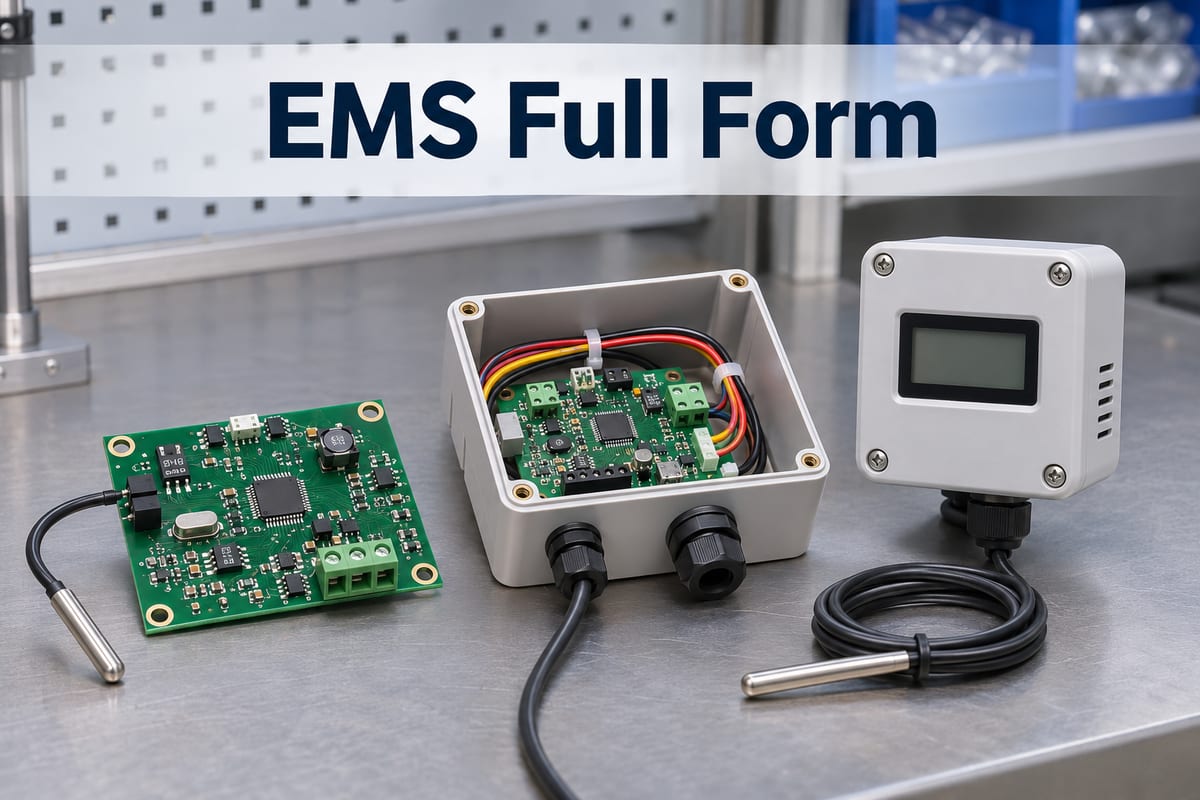
Populated circuit board, enclosure and finished temperature monitor
AI-generated physical illustration of board and product stages, not a Best Technology product photograph.

What Does an EMS Company Actually Deliver?

The deliverable depends on where the supplier’s work ends. A bare printed circuit board (PCB) has copper paths and pads but no installed electronic parts. Once the components are attached, you have a printed circuit board assembly (PCBA). Once the assembly is wired, installed in its enclosure and checked as a complete unit, you have a boxed product. Do not assume the third is included when you ask for the second.

Delivery stage What you receive
Bare PCB A fabricated board ready for components.
PCBA A populated board, with any specified inspection or board-level tests.
Box build An integrated unit with the agreed housing, wiring, configuration and final checks.

Engineering Support: Find Problems While They Are Still on Paper

The supplier starts with the circuit files, mechanical drawings, parts list and expected behavior. Design for manufacturability (DFM) checks whether the board can be made as drawn. Design for assembly (DFA) asks whether it can be put together; for example, can a worker plug in a cable without hitting the housing wall? Design for testability (DFT) asks how the finished work can be checked. In the monitor example, adding an accessible test point may make it possible to check the power rail before the board goes in its case. The output is a list of issues to resolve, not automatic approval to redesign the product.

PCB Fabrication: Turn the Drawing Into a Bare Board

Fabrication creates the board that holds and connects the components. Manufacturing files define where copper should remain and where the board is drilled or cut. The board drawing also identifies such requirements as thickness, material and layer construction. The output at this stage is a bare board, not a working monitor. An EMS supplier may fabricate it or coordinate a separate board shop; clarify who is responsible for the board specification and acceptance.

Component Sourcing: Buy the Parts That Match the Design

A bill of materials (BOM) tells the buyer which parts are needed. A manufacturer part number identifies a specific part more reliably than a short label such as “temperature sensor.” The buyer checks the part number, availability and approved alternatives. If the specified sensor is unavailable, a different one may have a different pinout or report readings in a format the firmware does not understand. A proposed substitute needs approval before it is used.

PCB Assembly: Attach the Parts to Make a PCBA

Surface-mount technology (SMT) attaches parts to pads on the board surface. A common route prints solder paste, places components and heats the assembly so the solder makes joints. Through-hole technology (THT) puts component leads through holes; those leads can then be soldered using the agreed process. The monitor could use SMT for its sensor and controller, and through-hole assembly for a terminal block. The output is the populated board, which still needs the agreed checks.
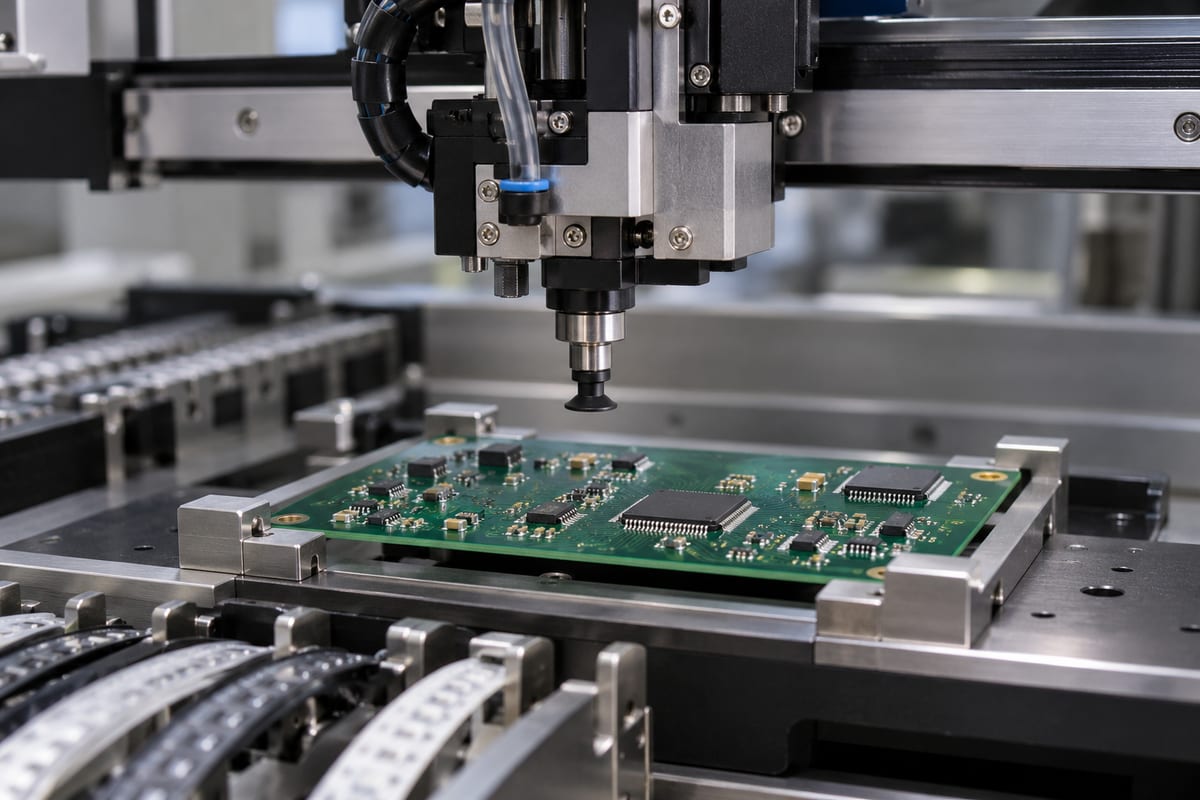
Automated placement head above a PCB during assembly
AI-generated illustration of PCB assembly, not a photograph of a Best Technology production line.

Inspection and Testing: Check the Build and the Behavior

A camera can help spot whether a visible part is missing or installed backward. It cannot tell whether the monitor reports the right temperature. To check that, use a defined sensor input or a controlled reference condition and compare the output with the approved test limits. The methods below complement one another; the right combination depends on the product and the test plan.

Method Example of what it checks
Solder paste inspection (SPI) Whether deposits are present and within the programmed limits before placement.
Automated optical inspection (AOI) Selected visible placement, orientation or joint features.
X-ray inspection Selected hidden features that cannot be seen directly, subject to the technique and geometry.
In-circuit testing (ICT) Selected connections or electrical properties at accessible points.
Functional testing Whether the board or unit responds as specified to a known input.

Box Build and Delivery: Make the Board Into a Product

Box build means integrating the board into the product. For the monitor, that could mean attaching a sensor cable and display, fixing the assembly in the case, loading approved firmware, checking the complete unit and applying a serial label. A board that passed its bench test might still fail after installation if the display cable is not seated. The final acceptance plan should say what to check after assembly, which records to keep and what is included in the shipment.
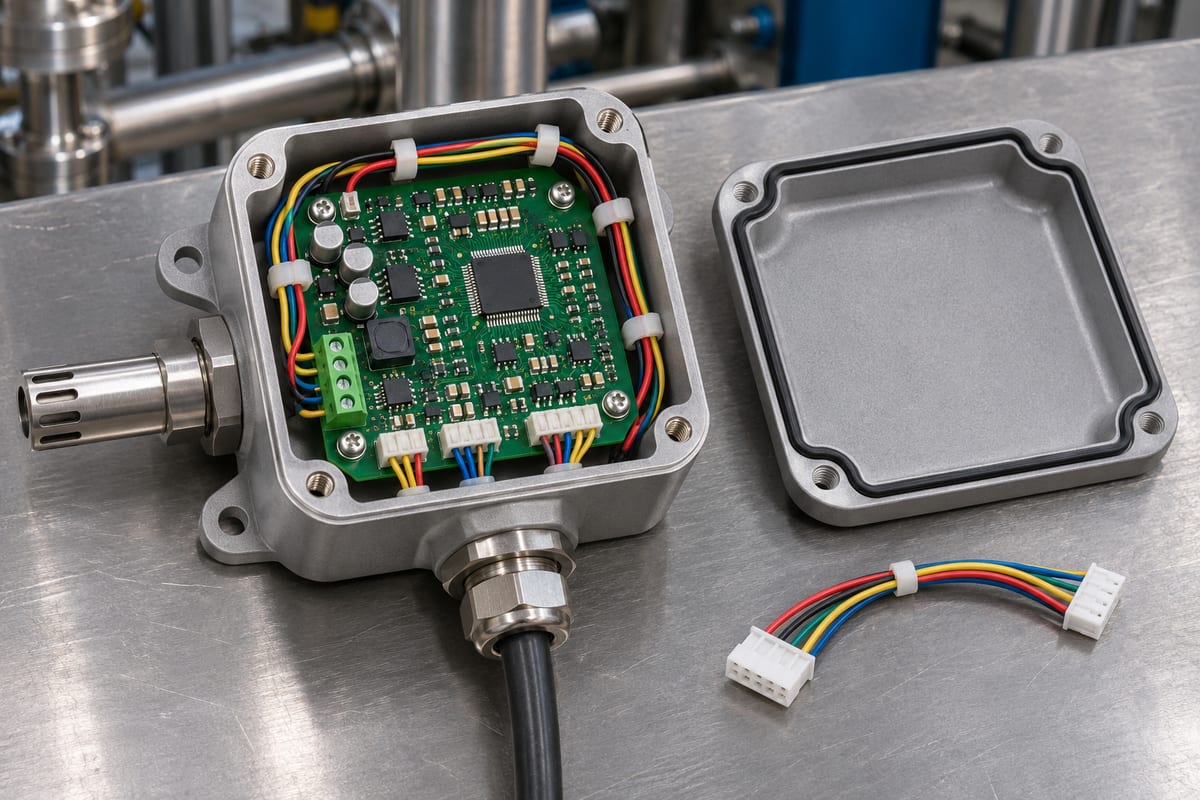
Populated PCB and cable harness inside an open instrument housing
AI-generated box-build illustration, not an actual customer unit or inspection record.

How the Work Moves From Prototype to Production

New product introduction (NPI) is the work of turning a new design into a repeatable build. In the example, the team reviews the files, builds samples, tests the monitor, and fixes issues before ordering a larger lot. A pilot run checks the approved production steps and test setup on a limited build. Use the same released revisions for the board, parts list, firmware and test procedure. If the pilot reveals an unresolved fault, fix and verify it before scaling the affected process.

EMS, OEM and ODM: Who Does What?

EMS is the manufacturing service. OEM means original equipment manufacturer; usage varies, so establish which company owns the product requirements and releases the design. ODM means original design manufacturer, typically a supplier that contributes the product design as well as manufacturing. A company can perform several roles. For the monitor, the brand team might supply the design and hire an EMS provider to build it. If the supplier provides a design platform for customization, the arrangement can be closer to ODM. Record who can approve design, part and firmware changes.

Turnkey, Consigned and Partial Turnkey: Who Buys the Parts?

These models tell you how material purchasing is divided. They do not determine whether a case, firmware or final test is included.

Model How it works in the monitor example
Turnkey The supplier buys the agreed boards and components. Confirm exclusions.
Consigned The customer sends the agreed materials; the supplier assembles them.
Partial turnkey The customer sends the specified sensor; the supplier buys the other agreed parts.

Quality Requirements: What Counts as a Pass?

A quality management system describes how an organization controls its work; it is not a pass result for your individual monitor. Product requirements describe what the specific build must meet. For example, IPC’s assembly acceptability guidance distinguishes assembly workmanship criteria from requirements for soldered assemblies. Agree on the applicable documents, revisions and acceptance criteria. Separately define the monitor’s test input, allowed output range and recorded results. Do not treat a general certification or a photograph of a test station as evidence that this unit passed.

How to Choose the Scope You Actually Need

Outsourcing can give a product team access to manufacturing resources without setting up its own line. The value depends on which tasks the supplier can perform and verify for this particular design. If you already own the components and can install the boards yourself, you may only need assembly and a board-level test. If you need an integrated monitor, also define the housing, harness, firmware, labels and final checks. Send the drawing, BOM, expected quantity and test requirements to sales@bestpcbs.com to discuss a Best Technology build.

FAQ

Is EMS the same as PCB assembly?

No. PCB assembly attaches the parts to the bare board. EMS can include that work plus procurement, engineering review, testing or product integration. The supplier may offer several of these services but perform only those agreed for your order. Confirm the delivery stage before comparing two proposals.

Do all EMS companies fabricate their own bare boards?

No. Some suppliers make boards, and others source them from a separate fabricator. Either model can work if the drawing, revision, material requirements and incoming checks are clear. Ask who places the board order and who investigates a board issue before the material enters assembly.

Does turnkey EMS include the enclosure?

Not necessarily. Turnkey may refer to sourcing and assembling the parts for a board, without a case or final product integration. List the enclosure, harness and other mechanical parts separately and state who provides each one. Also confirm whether the final check takes place after the unit is assembled.

Can I send only the critical components?

Yes, if the supplier agrees to partial turnkey. Mark each customer-supplied part on the BOM and agree what documents, quantities and packaging are required. Confirm how shortages or rejected parts will be handled, so the team does not assume the supplier will buy replacements without permission.

Can EMS include product design?

Some providers offer design services, but they are not automatic. A manufacturing review may identify a problem without including responsibility to redesign or qualify the product. Define the requested engineering deliverables and approval owner so changes to the circuit, mechanical design or firmware do not become ambiguous.

Does a passed board test mean the finished product works?

Not always. A board test may not cover connections, firmware settings or mechanical integration introduced later. Decide which behaviors require testing after the board is installed. For the monitor example, checking the display and sensor response in the finished unit can reveal a problem that the board-only test did not cover.

Who owns the test fixture and its software?

The parties should agree this before building it. Clarify who pays for the fixture, who supplies the test software, and who maintains, updates and can reuse them. Ask for the expected test records too. Ownership of the product design does not automatically answer these practical fixture questions.

What should I send before the first EMS build?

Start with the released fabrication and assembly files, the BOM with manufacturer part numbers, quantity, delivery form and the required tests. Add mechanical and firmware instructions if the work includes integration. Mark unresolved requirements explicitly so neither team mistakes a placeholder for an approved production instruction.
You may also like

EBest Circuit Showcases Soldering Expertise at the 10th QUICK Cup Competition
Wednesday, October 28th, 2026

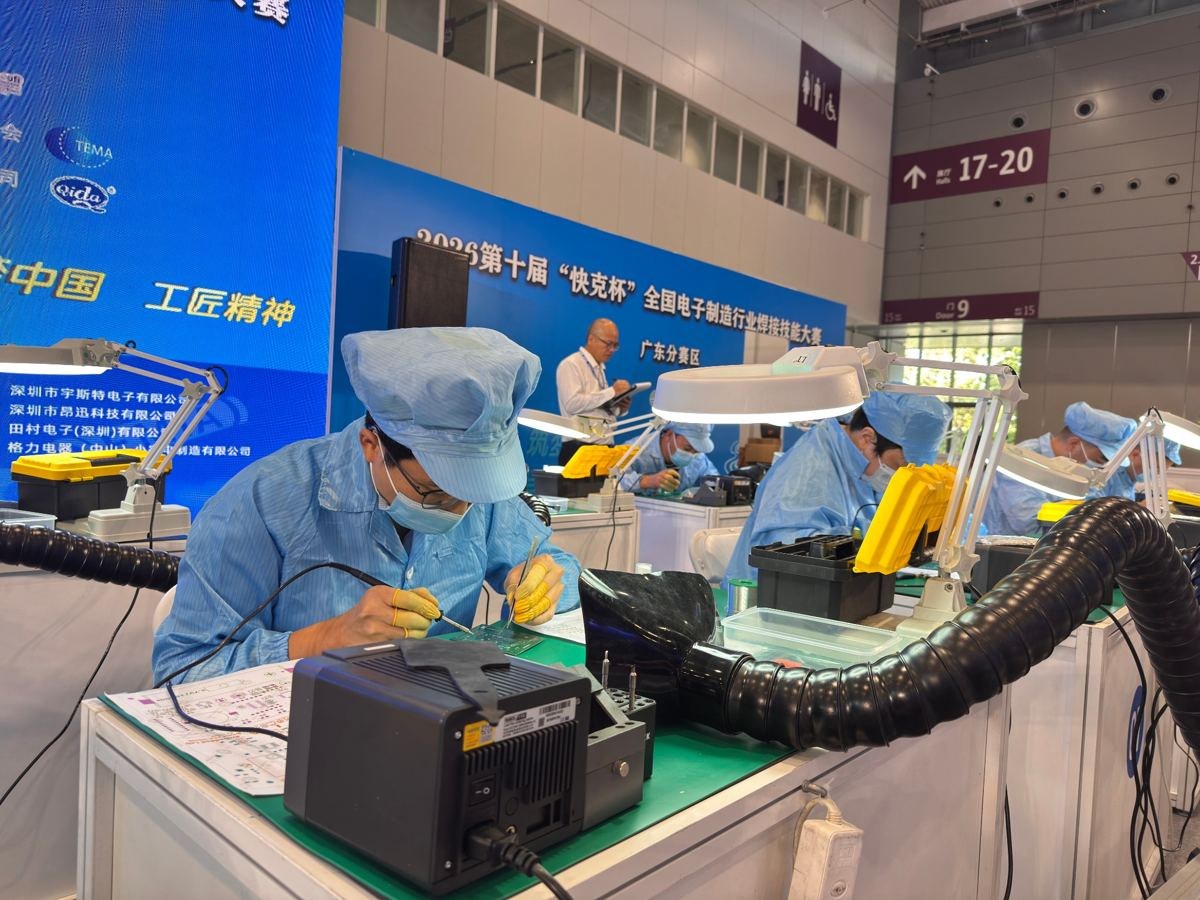
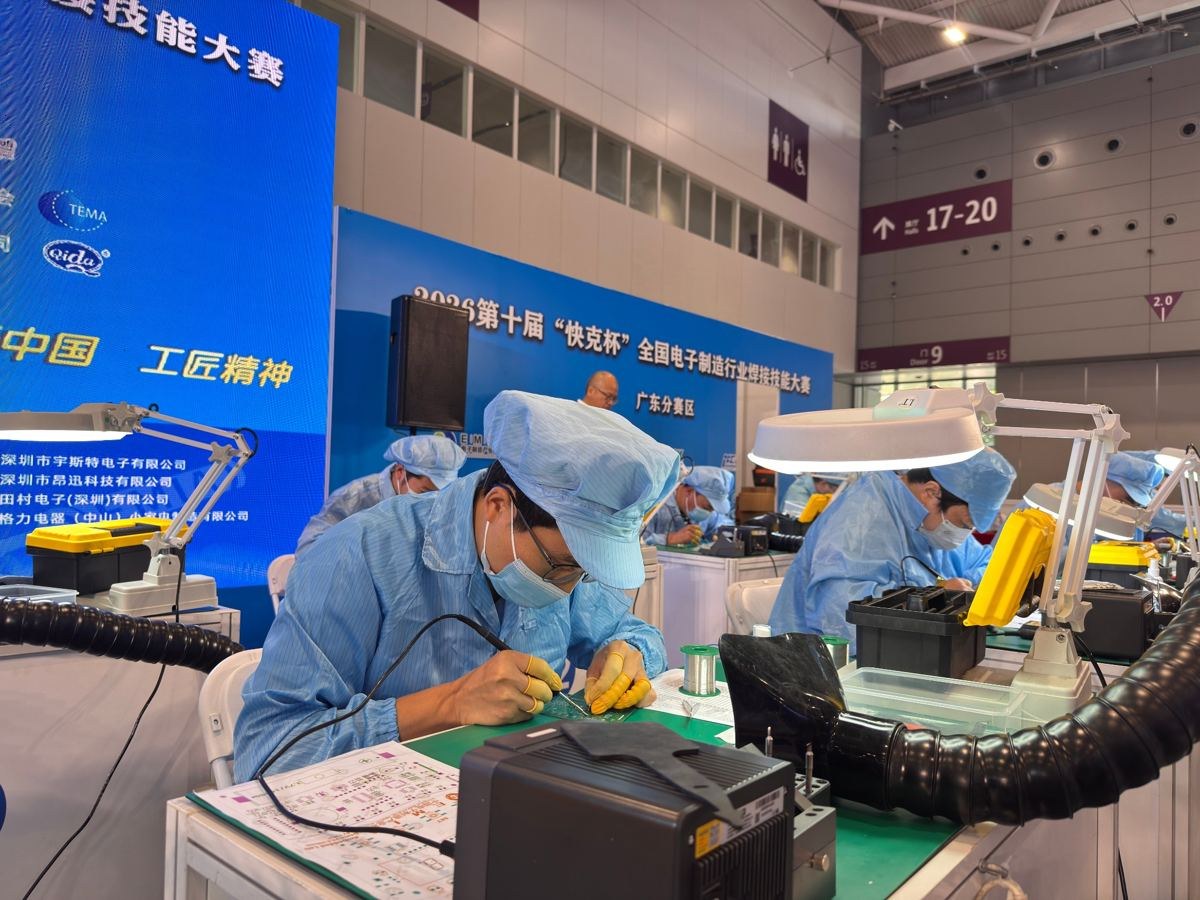
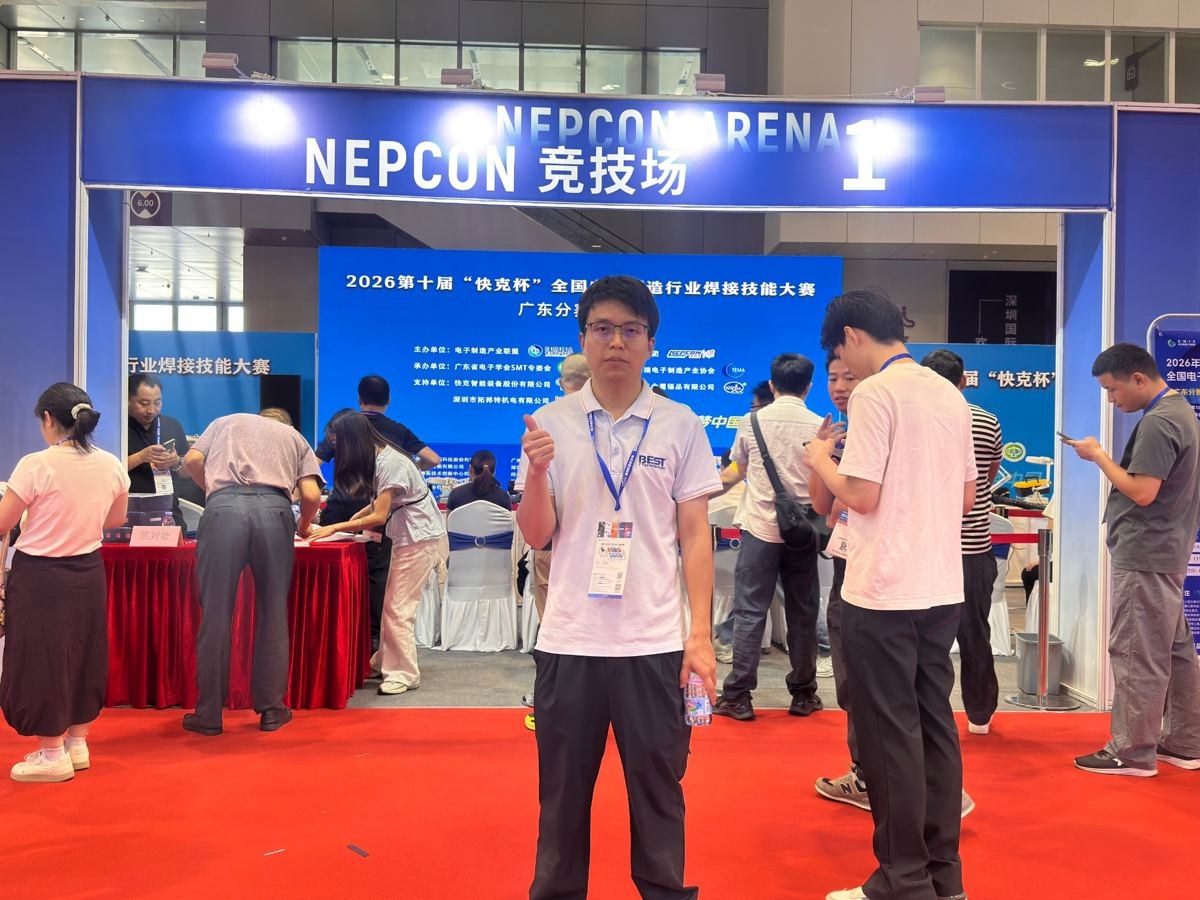
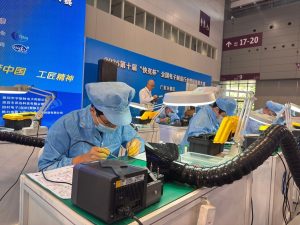
October 27, 2026 – EBest Circuit participated in the Guangdong regional round of the 10th QUICK Cup National Electronics Manufacturing Industry Soldering Skills Competition. The event brought together skilled technicians from across the electronics manufacturing industry to demonstrate their soldering expertise, exchange practical experience, and improve their technical abilities.

Technicians competing at the 10th QUICK Cup soldering skills competition

Key Takeaways

  • Our team participated in the Guangdong regional round of the 10th QUICK Cup soldering skills competition.
  • The event tested practical soldering precision, temperature control and joint formation.
  • We support PCB fabrication, component sourcing, assembly and project-specific inspection and testing.

Our Team at the QUICK Cup Soldering Competition

During the competition, our employees demonstrated their hands-on soldering skills through tasks requiring precision, steady control, and attention to detail.

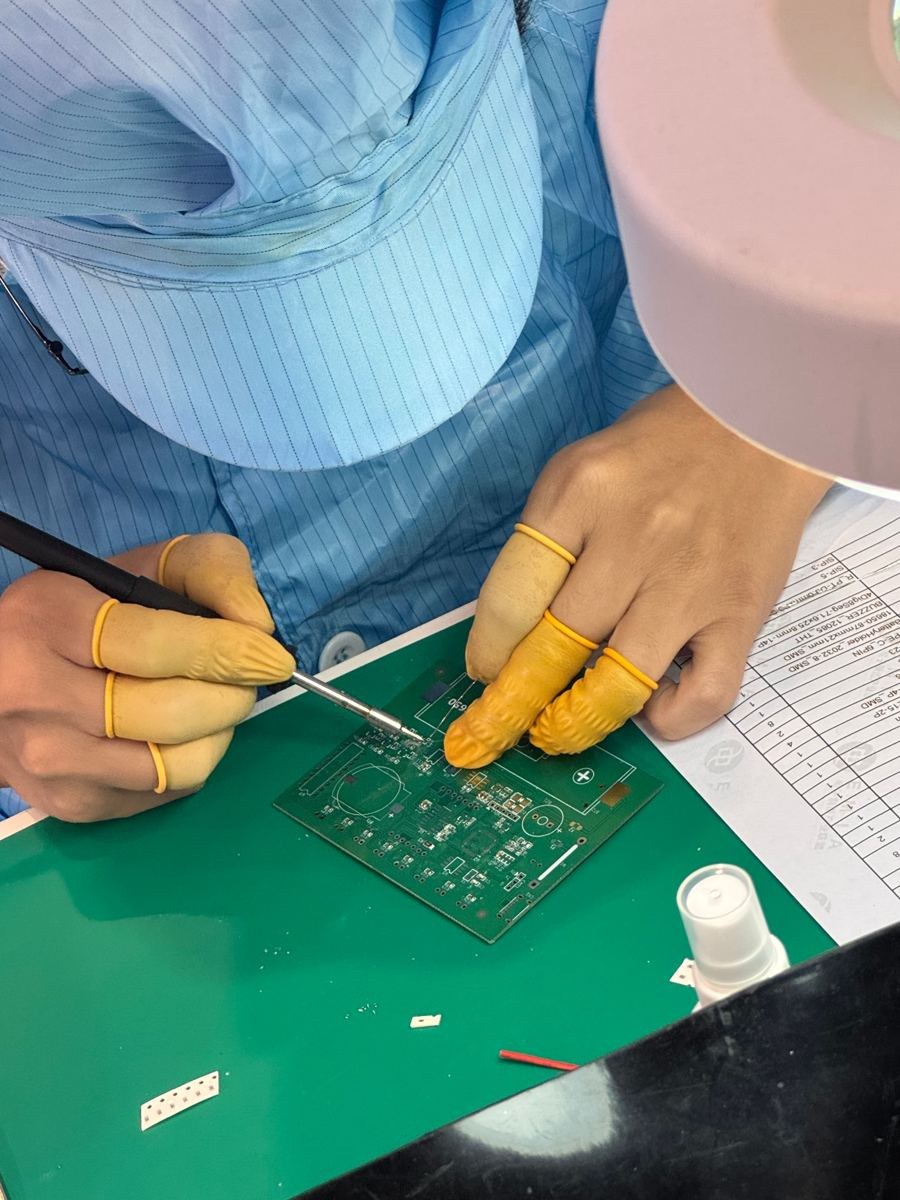
From soldering temperature control to solder joint formation, every step required practical experience and careful execution. Our team members approached the challenges with focus and professionalism, reflecting the workmanship they apply in daily PCB assembly production.

Close-up of manual PCB soldering during the QUICK Cup competition

The competition also offered a valuable opportunity to learn from industry peers, explore different soldering techniques, and further develop practical manufacturing skills.

Our PCB Manufacturing and Assembly Capabilities

At EBest Circuit, we believe advanced equipment and skilled technicians work together to achieve consistent manufacturing quality. That is why we encourage employee training, technical exchanges, and participation in professional skills competitions.

With 20 years of experience in electronics manufacturing, EBest Circuit provides comprehensive PCB fabrication and PCBA assembly services, including:

  • PCB Manufacturing: FR4, HDI, flexible PCB, rigid-flex PCB, metal core PCB, and ceramic PCB.
  • SMT Assembly: Four SMT production lines supporting fine-pitch components, BGA, and complex PCB assemblies.
  • DIP & Soldering: Through-hole assembly, wave soldering, selective soldering, and manual soldering.
  • Quality Inspection: SPI, AOI, X-ray inspection, ICT, and functional testing based on project requirements.
  • Turnkey PCBA Services: Component sourcing, PCB fabrication, assembly, testing, and box-build integration.
Technician performing soldering work at the QUICK Cup electronics manufacturing competition

Our quality management systems include ISO 9001, ISO 13485, IATF 16949, and AS9100D, supporting manufacturing requirements across medical electronics, automotive, industrial control, and other demanding applications.

How We Improve Skills and Manufacturing Quality?

Participating in the QUICK Cup reflects EBest Circuit’s commitment to employee development and continuous manufacturing improvement. By combining practical experience, professional training, and advanced production capabilities, we continue to strengthen our team’s technical expertise.

Behind every reliable PCB assembly is a team that cares about every detail.

EBest Circuit employee at the QUICK Cup soldering competition

Whether you need PCB prototypes, low-volume PCBA, or volume production, EBest Circuit is ready to support your project with engineering assistance, manufacturing, and quality control.

For PCB and PCBA quotations, feel free to contact us at sales@bestpcbs.com.

You may also like

How Does PCB to PCB Soldering Create Reliable Board Connections?
Wednesday, October 28th, 2026

PCB to PCB soldering joins compatible conductive features on two circuit boards into a permanent electrical connection. A castellated module can sit directly on matching carrier-board pads, while soldered pins can connect boards at a defined spacing. Reliability starts with the joint geometry, access for heating and inspection, and a mechanical support arrangement that does not ask small solder joints to carry the entire assembly.

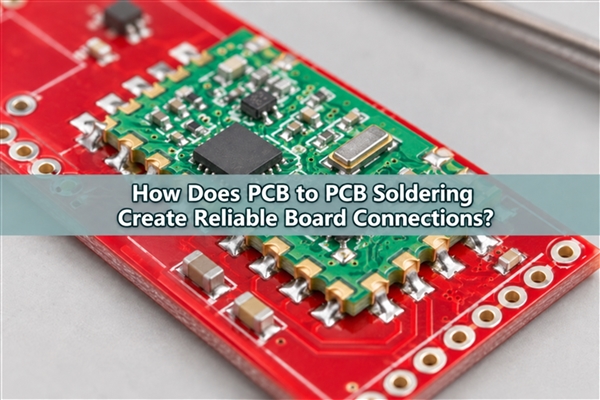
AI illustration of a castellated PCB module soldered onto a matching carrier board

Can You Solder One PCB Directly to Another?

Yes, when both boards have solderable features intended to meet. Plated half-holes around a module edge are a common example: each half-hole aligns with a carrier land, and solder connects the exposed plating to that land. Two arbitrary board edges covered in solder mask will not form the same connection.

Decide whether the connection needs to be permanent before choosing the layout. A soldered module can reduce connector height and part count, but replacing it requires controlled rework. A separable board-to-board connector is generally more practical where routine servicing or repeated removal is part of the product requirement. Direct soldering also leaves less freedom to accommodate footprint errors after fabrication.

Which Connections Are Suitable for PCB to PCB Soldering?

The relevant types of PCB soldering depend on how the two boards meet. Start with board orientation, service access and mechanical loads, then select the joining process. A continuous solder bead along unrelated board edges is not a substitute for a designed interconnect.

Connection Suitable arrangement What the design must provide
Castellated module Small module mounted flat on a carrier Matched lands, controlled placement, solder access and required underside clearances
Soldered pins or headers Boards separated vertically or joined at an angle Compatible holes and pins, spacing control, access to each soldered end and support
Designed edge or tab joint Fixed board geometry with exposed joining lands Defined copper geometry, a locating fixture and a validated load path
Flex termination soldered to a rigid board Low-profile flexible interconnect Purpose-designed exposed fingers, alignment support and strain relief outside the joint

When soldering header pins to PCB holes on both boards, hold the boards at the specified spacing while the joints solidify. Confirm access to both ends before choosing this construction. Short wire links are another option when the board positions cannot be matched directly. They require strain relief and routing space, and they are not equivalent to a compact surface-mounted module. For high-speed signals or substantial current, evaluate the complete connection path rather than assuming that fewer parts automatically means better performance.

How Do Castellated Holes Connect a Module to a Carrier Board?

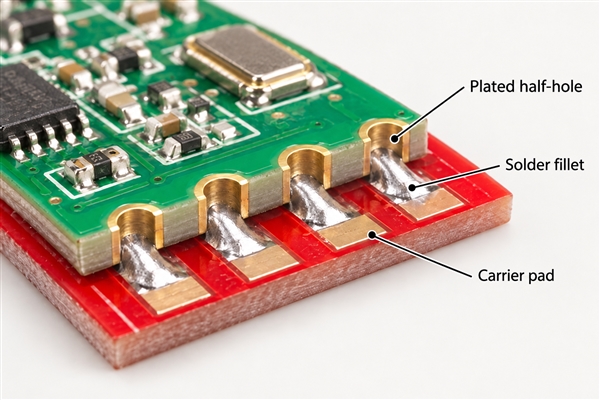
Castellated holes are plated holes intersected by the finished PCB edge. Their exposed, curved copper walls provide solderable surfaces beside the module. The carrier’s land extends into the matching connection region so solder can wet both surfaces. The visible outside fillet provides useful inspection access, although it cannot reveal every hidden interface beneath the module.

Technical illustration identifying a plated half-hole, solder fillet and carrier pad

Half-hole plating quality, edge definition and land registration matter before assembly starts. A damaged or poorly plated edge cannot be corrected simply by adding more solder. For a new module design, specify the finished outline and half-hole requirements together with the carrier footprint; do not derive production dimensions from a photograph.

On FR4 PCBs, board thickness, copper distribution and surface finish also affect how the joint heats and wets. The module manufacturer’s recommended land pattern remains the starting point when using an existing module.

How Should the Two PCB Footprints Be Matched?

Compare both coordinate systems, not just the nominal pitch. Check pin 1, rotation, row spacing, board outline tolerance, pad dimensions and any module features extending underneath. A footprint that appears correct from above can still put copper beneath an antenna keepout or interfere with a bottom-side component.

  • Use the current module drawing and its specified carrier land pattern.
  • Check solder-mask openings and whether the module sits flat without unintended contact.
  • Allow tool and inspection access around the perimeter.
  • Review routing, copper balance and large ground connections that change local heat demand.
  • Keep antenna, exposed-contact and mechanical keepouts consistent across both drawings.
  • Provide fiducials or other suitable placement references for the assembly process.

Do a dry fit before soldering prototypes. If one end aligns but the other does not, stop and investigate dimensions or orientation. Pulling a board into place with solder can leave misregistration or residual stress that becomes visible only after cooling.

How Do You Hand-Solder Two PCBs Together?

Hand soldering is useful for accessible castellated joints and prototypes. The essential PCB soldering techniques are controlled alignment, heating both mating surfaces and limiting solder volume. Use a stable holder, magnification, appropriate fume extraction and an ESD-controlled setup for sensitive assemblies. Disconnect all power and batteries.

  1. Inspect the lands and half-holes for damage or contamination. Use a cleaning method compatible with the board and components.
  2. Place the module in its intended orientation and apply compatible flux where needed.
  3. Tack one accessible corner with a small amount of solder, then verify the entire footprint before fixing the opposite side.
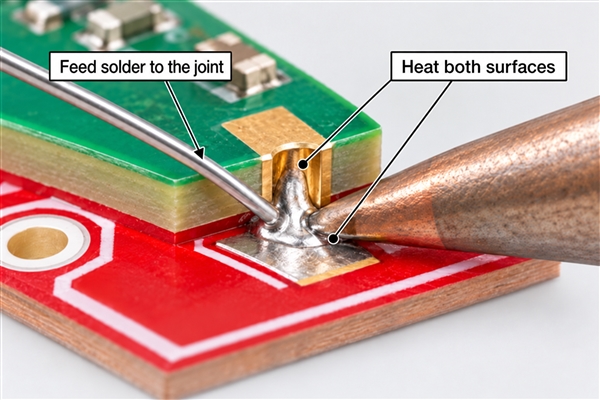
  4. Place the PCB soldering iron tip so it transfers heat to both the carrier land and the module’s plated edge.
  5. Feed a controlled amount of solder to the heated joint. Withdraw the solder wire, then the tip, and let the joint solidify without movement.
  6. Complete the remaining connections, checking alignment and bridges as work progresses.
  7. Clean residues only as required by the flux chemistry and product process, then inspect and test.
Technical illustration showing heat applied to both mating surfaces and solder fed into the joint

Choose solder wire for PCB soldering with an alloy, flux core and diameter appropriate to the joint. A large wire can make small deposits difficult to control. Do not use plumbing flux on electronic assemblies. If the tip cannot reach both surfaces, redesign the access or use a suitable assembly process instead of heating nearby components for an extended time.

A PCB soldering kit marketed for soldering circuit boards for beginners may supply an iron and wire without suitable magnification, holding support or a correctly sized tip. Check those requirements separately, and practice the same joint geometry on scrap or training boards before handling a valuable module.

When Should You Use Reflow Soldering for PCB Modules?

Reflow is appropriate when the module is qualified for that process and the carrier layout supports repeatable paste printing and placement. It can join many connections in one controlled cycle, including connections that are impractical to hand-solder. The module and every already-installed component must tolerate the planned thermal exposure.

Specify paste deposit requirements through the SMT stencil design rather than treating the stencil as a copy of the copper artwork. Aperture geometry and stencil thickness influence deposited volume, bridging and module seating. Inspect the print and placement before reflow; an oven cannot correct a misaligned footprint.

A PCB soldering machine setpoint alone does not establish a valid profile. Measure the loaded assembly and examine both the thermally heavy joints and heat-sensitive locations. Count earlier reflow operations on the module, not only the carrier’s latest pass. Follow the actual module’s limits for reflow exposure, moisture handling and orientation.

What Temperature Should You Use for PCB to PCB Soldering?

There is no single temperature that applies to every two-board assembly. For hand soldering, the iron setpoint is a tool setting; the joint temperature depends on tip contact, tip size, thermal recovery, copper area and heating time. A very fine tip may transfer heat poorly to a large ground connection even when its setpoint is high.

For reflow, use the solder paste’s recommended process window within the limits of the module, laminate and other components. Peak temperature, time above the alloy’s liquidus, ramp and cooling conditions all matter. Do not transfer a temperature from a different alloy or module into a production instruction without qualification.

When a joint heats slowly, first check contact area, tip condition, flux activity and the thermal load. Raising temperature repeatedly can damage pads or components without fixing the root cause. Where preheating is appropriate, control it as part of the complete process and verify the actual assembly temperature.

Can You Solder Flex PCB to Rigid PCB?

Soldering flex PCB to rigid PCB is possible when the flex has exposed termination features designed for the connection. The flexible dielectric itself is not solderable. Finger pitch, coverlay opening, surface finish and support near the termination must suit the selected hand, reflow or specialized joining process.

Keep the intended bend away from the soldered transition. Solder wicking into a flexible conductor can create a locally stiff region, concentrating strain at its end. A fixture or stiffened termination can maintain alignment during joining, while the product’s strain relief controls movement afterward. Do not repeatedly flex a finished joint to demonstrate that the cable is flexible.

A purpose-designed rigid-flex board can remove a separate soldered interface, but it changes the board construction and cost. A connector may be preferable when the flex must be replaced. Choose among these options before committing to a footprint, not after assembly problems appear.

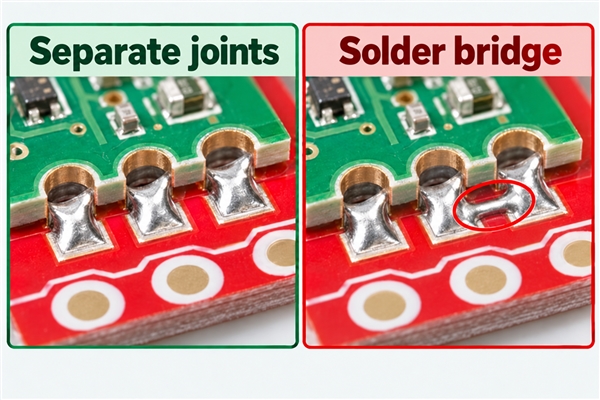
How Can You Prevent Solder Bridges and Poor Wetting?

Inspect the geometry and process together. Excess solder, shifted placement, unsuitable paste deposits and closely spaced lands can create bridges. Oxidized or contaminated surfaces, exhausted flux and inadequate heat transfer can prevent wetting. Adding flux is not a reliable repair for missing plating or a lifted pad.

Observation First checks Controlled response
Solder connects neighboring lands Placement, deposit volume, land spacing Remove the bridge using a qualified rework method, then inspect for damage and shorts.
Solder beads up instead of wetting Surface condition, flux compatibility, actual heat transfer Identify the cause before reheating; replace damaged material when necessary.
Module sits tilted Underside interference, uneven deposits, first tack position Correct seating through controlled rework; do not force the board flat after solidification.
Land or plating lifts Thermal exposure and mechanical force Stop rework and assess conductor integrity against an approved repair disposition.

A matte joint is not automatically a cold joint, particularly with lead-free alloys. Evaluate wetting, connection geometry and evidence of disturbance against the specified acceptance criteria rather than demanding a uniformly shiny appearance.

How Should PCB-to-PCB Solder Joints Be Inspected?

Start with orientation and seating, then inspect every accessible joint for bridging, wetting, damage and contact with unintended conductors. Use magnification and lighting that reveal the module edge rather than hiding it behind reflections. Record the location of a suspect joint so rework and retest remain traceable.

Technical illustration comparing separated castellated solder joints with an unwanted bridge between adjacent pads

Follow visual inspection with the electrical tests appropriate to the circuit. Check for unintended supply shorts before first power-up, then use a controlled power-on procedure and the agreed functional test. Continuity alone cannot show that a mechanically weak joint will survive service, and a powered module that starts once has not passed environmental reliability testing.

At EBest Circuit (Best Technology), our PCB assembly services include solder-paste inspection, AOI, X-ray inspection and functional testing. We use equipment including the SINIC-TEK S8080 3D SPI and UNICOMP AX8200 X-ray system. The inspection route depends on joint accessibility and the assembly: optical inspection cannot see through a module, and X-ray does not replace electrical or mechanical validation.

How Do You Keep Mechanical Loads off the Solder Joints?

A daughterboard can act as a lever. Connector insertion, cable pull, vibration and enclosure bending may load its soldered connections even when the module weighs very little. Place supports so these forces reach the chassis or carrier structure without being concentrated at the outermost joint.

Use the module’s approved mounting features, standoffs or an appropriate retention arrangement where the design requires them. Supports must respect electrical clearances, antenna keepouts and component height. An incorrectly positioned support can bow the board or impose stress instead of relieving it.

Thermal expansion also matters. Two boards with different temperatures, sizes or constructions can move relative to each other during operation. Evaluate the final supported assembly under its actual thermal and mechanical requirements. An unsupported desktop prototype is not evidence for a product exposed to repeated vibration or temperature cycling.

What Files Do We Need to Assemble Your PCB Module?

Send us the carrier fabrication data, assembly drawing, BOM, placement data and the module’s current drawing and assembly instructions. Identify customer-supplied modules and include their part revision, packaging and available moisture or reflow history. For a custom two-board connection, include both board drawings and the intended assembled position.

For PCB to PCB soldering, specify the required support arrangement, solder alloy, inspection criteria and functional-test procedure. If a joint will be hidden after enclosure assembly, identify when it must be inspected. These details let us evaluate the footprint and process before boards and modules reach the assembly line.

We provide PCB fabrication together with PCB assembly and soldering, component sourcing and engineering review matched to the project. Our placement capability includes SMD packages down to 01005 and BGA pitch down to 0.25 mm, subject to the specific layout and process review; these figures are not automatic minimums for a castellated module. Contact sales@bestpcbs.com with your drawings and quantities for a PCB-to-PCB assembly quotation.

PCB to PCB Soldering FAQs

How to Clean a PCB after Soldering?

Match the cleaning process to the flux and the module’s component restrictions. Residue trapped beneath a module may be difficult to remove and dry. Do not assume that an alcohol wipe cleans hidden areas or that every populated module can be immersed. Specify whether the assembly uses a qualified no-clean process or a validated cleaning and drying process.

Can a soldered PCB module be removed and reused?

Sometimes, but removal must stay within the module’s rework limits. Heating all required joints without prying is important. Inspect the module and carrier after removal, and do not assume that an apparently intact module remains suitable for reuse without the required checks.

Can conductive glue replace solder between two PCBs?

Not as a direct substitute in a solder-qualified footprint. Conductive adhesives have different curing, electrical, mechanical and environmental behavior. Using one requires a joint design and qualification appropriate to that material.

Does a continuity beep prove the connection is good?

No. It shows that the meter detected a conductive path under its test conditions. Parallel circuit paths can also affect the reading. A continuity check does not establish wetting quality, current-carrying performance or long-term mechanical reliability.

You may also like

EBest Circuit at Canton Fair 2026: PCBA Highlights and What’s Next
Tuesday, October 20th, 2026

The five-day exhibition has successfully concluded for EBest Circuit at Canton Fair 2026 Autumn.

From October 15 to 19, 2026, our team welcomed visitors at Booth 16.3H18 in Area C of the China Import and Export Fair Complex in Guangzhou. This year, our exhibition focused on PCB assembly (PCBA), giving customers a closer look at our manufacturing capabilities, assembled circuit boards, quality systems, and electronics manufacturing services.

Throughout the exhibition, we had the opportunity to meet customers, engineers, purchasing teams, distributors, and business partners from different markets. Some visitors came with active PCB and PCBA projects. Others were looking for a new manufacturing partner or wanted to understand our capabilities in component sourcing, SMT assembly, inspection, testing, and complete electronics manufacturing.

To everyone who stopped by our booth: thank you for visiting EBest Circuit at Canton Fair 2026 Autumn.

EBest Circuit team at Canton Fair 2026 Autumn, Booth 16.3H18

What Happened at Booth 16.3H18 During Canton Fair 2026?

Canton Fair provided us with something that emails and online meetings cannot completely replace: face-to-face conversations around real electronics projects.

At Booth 16.3H18, our team introduced EBest Circuit, answered manufacturing questions, presented PCBA samples, and discussed new projects with visitors throughout the five-day exhibition.

Our discussions covered different stages of electronics manufacturing, including:

  • PCB fabrication
  • Component sourcing
  • SMT assembly
  • Through-hole assembly
  • Prototype PCBA
  • Volume production
  • AOI and X-ray inspection
  • Functional testing
  • Conformal coating
  • Cable assembly
  • Box-build assembly

Many conversations started with an assembled PCB on our display shelf and quickly moved into actual project requirements: board construction, component availability, inspection methods, testing, lead time, traceability, and production planning.

That is exactly what we hoped to achieve at the Canton Fair—not simply show products, but create an opportunity to discuss how those products are actually manufactured.

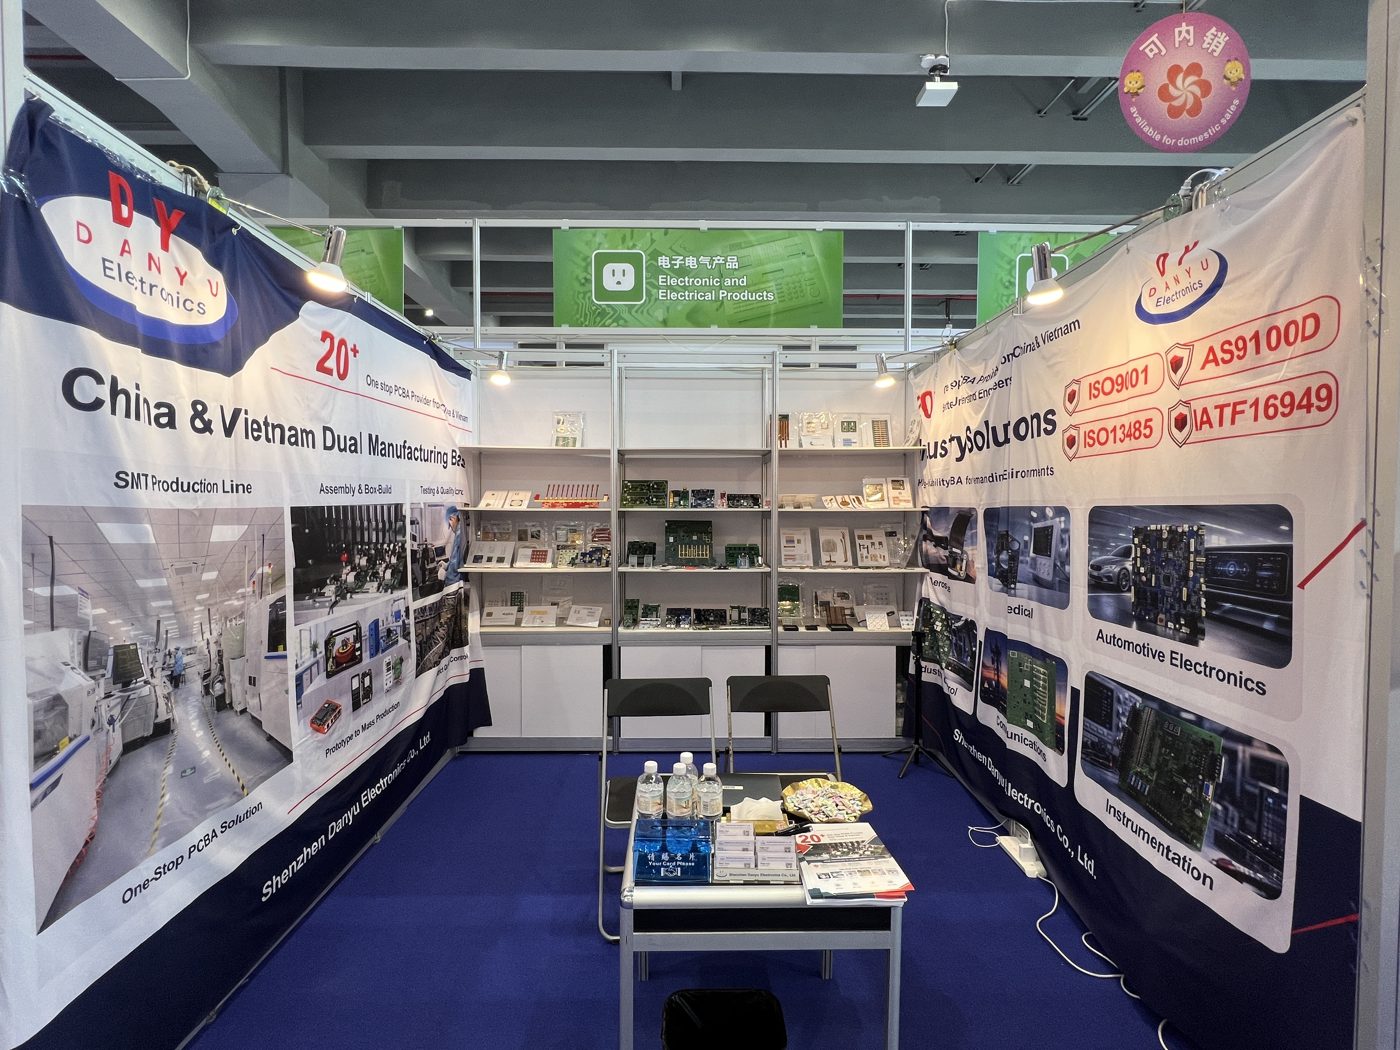
EBest Circuit PCBA exhibition booth at Canton Fair 2026 Autumn

Why Was PCBA the Main Focus of Our Exhibition?

Our main focus at Canton Fair 2026 Autumn was PCBA manufacturing.

Rather than showing only bare circuit boards, we displayed assembled boards and related samples so visitors could see the types of electronics manufacturing projects we support.

Our PCBA capabilities cover:

  • SMT PCB assembly
  • THT and mixed assembly
  • BGA, QFN and fine-pitch assembly
  • Double-sided PCBA
  • Flexible PCB assembly
  • Rigid-flex PCB assembly
  • Metal-core PCB assembly
  • Prototype and low-volume production
  • Medium- and high-volume manufacturing
  • Turnkey component sourcing
  • AOI and X-ray inspection
  • ICT and functional testing
  • Conformal coating
  • Cable and wire assembly
  • Box build

The circuit boards displayed at the booth represented different component densities, package types, connectors, PCB structures, and application requirements.

For many visitors, seeing an actual assembled board made the conversation much more specific. Instead of discussing manufacturing only in general terms, we could talk directly about BGA inspection, connector assembly, component sourcing, thermal requirements, testing, or production scaling.

Watch Our Canton Fair 2026 Autumn Highlights

For customers and partners who could not meet us in Guangzhou, we also recorded some moments from the exhibition. The video below gives a closer look at our presence at Canton Fair 2026 Autumn.

Which Industries Did We Discuss at Canton Fair?

One of the strengths of Canton Fair is the diversity of visitors. During the exhibition, we discussed PCB and PCBA manufacturing requirements for products used across several industries.

Industrial Electronics

Industrial automation, control equipment, sensors, monitoring systems, motor controls, and other industrial products often require stable long-term production and consistent assembly quality.

Automotive Electronics

Automotive projects place greater emphasis on process control, traceability, testing, and manufacturing consistency.

Medical Electronics

Medical-related electronics may require tighter documentation, controlled production processes, traceability, and quality management.

Communication Equipment

Communication products often combine dense component placement, connectors, RF circuitry, high-speed signals, and controlled-impedance PCB requirements.

New Energy and Power Electronics

Energy storage, charging equipment, power conversion, industrial power supplies, and similar products can involve demanding current and thermal requirements.

Aerospace and Aviation Electronics

Aerospace-related projects place particularly high importance on process control, documentation, traceability, and reliable manufacturing.

Meeting customers from these different industries also reminded us that there is no single manufacturing process that fits every PCBA. The board, components, application, operating environment, production quantity, and test requirements all influence how a project should be manufactured.

How Does EBest Circuit Support PCB-to-PCBA Manufacturing?

Another topic that attracted attention at our booth was our ability to support more than PCB assembly alone.

EBest Circuit supports a broad range of PCB technologies, including:

  • Multilayer PCB
  • HDI PCB
  • Flexible PCB
  • Rigid-flex PCB
  • Metal-core PCB
  • Heavy copper PCB
  • High-Tg PCB
  • High-frequency PCB
  • High-speed PCB
  • Impedance-controlled PCB
  • Ceramic PCB
  • Copper-based PCB

After PCB fabrication, projects can continue into component sourcing, stencil preparation, SMT, THT, inspection, programming, testing, conformal coating, cable assembly, and box build.

This gives customers the option to coordinate PCB and PCBA requirements through one manufacturing project rather than separating each stage among different suppliers.

For engineering teams, this can help PCB manufacturability and assembly requirements be reviewed together. For purchasing teams, it can simplify communication and reduce the number of suppliers involved in one project.

What Quality Systems and Certifications Support Our PCBA Production?

Visitors also asked about the quality systems behind our manufacturing capabilities.

EBest Circuit maintains certifications and compliance capabilities including:

  • ISO 9001
  • ISO 13485
  • IATF 16949
  • AS9100D
  • UL
  • RoHS
  • REACH
  • SGS

These certifications help us support customers across general electronics, industrial, automotive, medical, aerospace, communication, and other quality-sensitive applications.

Quality control also extends beyond certificates. Depending on the project, our production and inspection flow can include incoming material inspection, solder paste printing, SPI, SMT placement, reflow, AOI, X-ray inspection, through-hole assembly, electrical testing, functional testing, final inspection, and production records.

The inspection and testing plan is determined according to the actual board and customer requirements.

What Made Canton Fair 2026 Valuable for Us?

Products were displayed on the shelves, but the most valuable part of the exhibition happened in front of them.

It was the conversations.

Customers talked with us about new product development, existing supplier challenges, prototype quantities, component availability, production quality, testing requirements, and upcoming mass-production plans.

Some were beginning entirely new projects. Others were evaluating alternative PCB or PCBA suppliers.

Those conversations provide information that cannot always be found in a Gerber file or BOM. A drawing tells us what needs to be manufactured. A face-to-face discussion often tells us why a particular requirement matters to the finished product.

That understanding helps both sides communicate more efficiently once a project moves into engineering review and production.

Next Stop: Meet Us at Electronica 2026 in Munich

Our 2026 exhibition schedule is not over yet. After meeting customers and partners in Guangzhou, EBest Circuit will next attend Electronica 2026 in Munich, Germany. We look forward to continuing the conversations around PCB, PCBA, component sourcing, testing, and complete electronics manufacturing with customers in Europe and other international markets.

Exhibition: Electronica 2026

Date: November 10–13, 2026

Location: Munich, Germany

Hall: A1

Booth: 178

If you are planning to visit Electronica 2026, we invite you to meet our team at Hall A1, Booth 178. Bring your project requirements, Gerber files, BOM, or upcoming sourcing plans, and we can discuss your PCB and PCBA needs face to face.

From Guangzhou to Munich, our goal remains the same: to help customers move electronic products from design into reliable manufacturing with coordinated engineering and production support.

Thank You for Visiting EBest Circuit at Canton Fair 2026 Autumn

Canton Fair 2026 Autumn has come to an end for our team, but many of the conversations that started in Guangzhou are continuing.

We would like to thank every customer, engineer, purchasing professional, distributor, partner, and visitor who spent time with us at Booth 16.3H18.

Whether you stopped by to look at our PCBA samples, discussed a specific manufacturing project, or simply wanted to learn more about EBest Circuit, we appreciate your visit.

For customers who discussed projects with us during the exhibition, you are welcome to send the latest:

  • Gerber files
  • BOM
  • Pick-and-place files
  • Drawings
  • Production quantities
  • Testing requirements
  • Programming requirements

If you could not meet us in Guangzhou but are looking for a PCB and PCBA manufacturing partner, you can send your project information directly to sales@bestpcbs.com.

From PCB fabrication and component sourcing to PCBA, testing, conformal coating, cable assembly, and box build, EBest Circuit looks forward to supporting your next electronics project.

Thank you for meeting us at Canton Fair 2026 Autumn. See you at our next exhibition!

You may also like

Smart Meter PCB Manufacturing for Accurate Energy Measurement
Thursday, October 8th, 2026

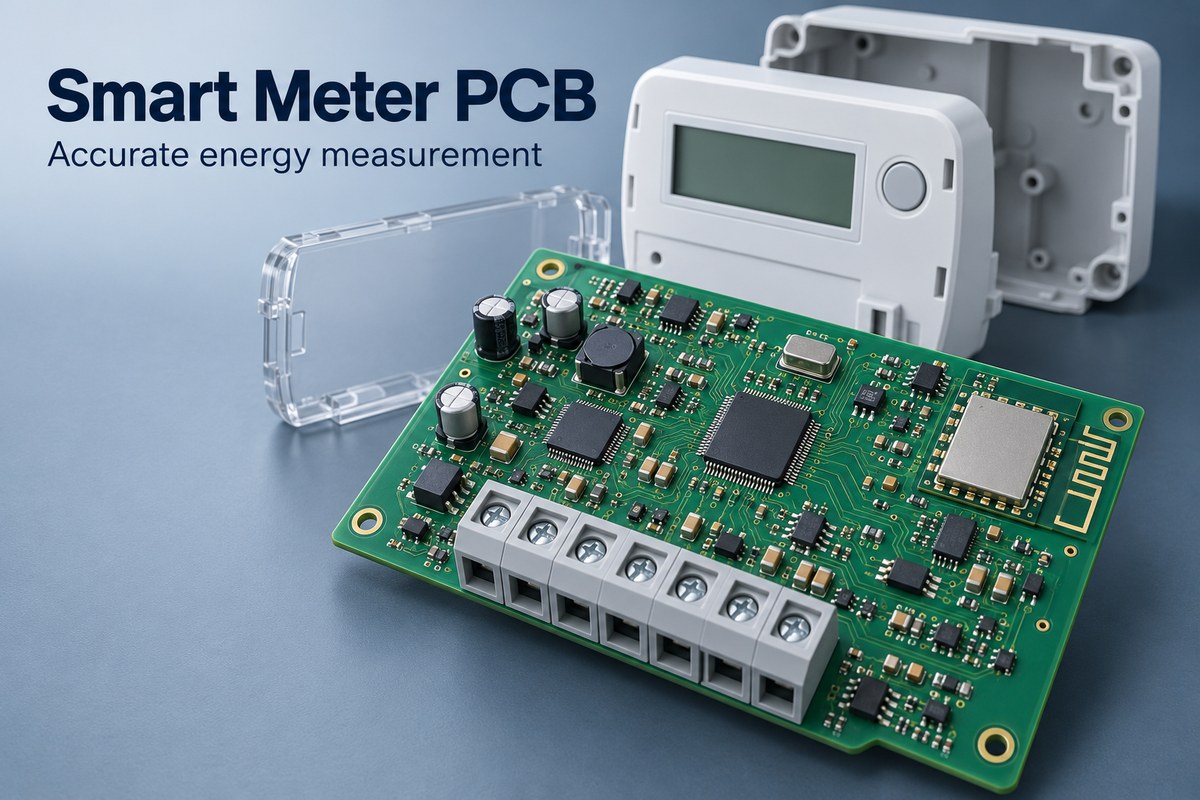
A smart meter PCB brings together the circuits that measure electricity consumption and transmit the readings. Inside a smart electricity meter, sensitive measurement signals share space with power supplies, processors, and communication hardware. Accurate readings depend on preserving those signals through PCB layout, assembly, and calibration.

EBest Circuit provides PCB fabrication and PCB assembly services for customer-approved designs, including mixed assemblies with SMT measurement circuits and through-hole power connections. Our team can coordinate board fabrication, component assembly, and agreed testing for prototype and production builds. Discuss your smart meter PCB project with us at sales@bestpcbs.com.

smart meter PCB

What Does a Smart Meter PCB Do?

A smart meter PCB connects the measurement circuit to the processing, storage, and communication electronics. Once assembled with components, it supports a clear signal path.

Voltage and current sensing → signal conversion → energy calculation → storage and communication

Voltage and current sensors produce signals that the analog front end and analog-to-digital converter can process. A metering IC or processor uses the samples to calculate power and accumulated energy. Memory retains readings, while communication hardware transfers data to other equipment or a utility network.

Power supplies, protection circuits, clocks, and display interfaces support this path. The communication interface enables remote data exchange; a digital display alone does not make a meter smart.

These functions can share one PCB or occupy separate metrology and communication boards. Separate boards allow communication options to change without replacing the entire metrology board, although their connectors and power interfaces still need to work together.

How Do Current Sensors Affect Metering Accuracy?

Current sensors influence both the amplitude and timing of the signal entering the metering circuit. An accurate ADC cannot recover information already distorted by sensor heating, phase shift, or saturation.

Current Sensor How It Measures Current Sources of Measurement Error
Shunt resistor Measures the voltage across a known resistance Resistance tolerance, self-heating, temperature drift, and connection resistance
Current transformer (CT) Converts alternating primary current into a secondary signal Ratio error, phase shift, burden, and core saturation
Rogowski coil Produces a signal proportional to the rate of current change, which is then integrated Coil characteristics, positioning, and integration accuracy

For a shunt, V = IR describes the sensing voltage, while P = I²R describes the heat generated. A higher resistance gives a larger signal at the same current, but also produces more heat. That temperature change can affect the resistance and the resulting measurement.

Phase error changes the relationship between the measured voltage and current signals, affecting active power calculation. Calibration can correct characterized gain and phase errors. It cannot reconstruct a clipped waveform or make a saturated sensor behave linearly.

How Does Smart Energy Meter PCB Design Keep Measurement Signals Stable?

The layout must preserve the intended sensing voltage while keeping switching and communication currents out of its measurement path. Three connections deserve particular attention.

  • Take shunt measurements from the intended sense terminals. Kelvin connections separate the voltage-sensing traces from the load-current connections. If the sense traces pick up additional voltage drop along a current-carrying connection, the ADC measures more than the shunt voltage.
  • Keep filtering and decoupling close to the circuits they serve. Input filters must match the metering IC and sampling requirements because they affect amplitude and phase. Short local decoupling connections help keep supply disturbances from reaching sensitive circuitry.
  • Give return currents a suitable path. Digital clocks, switching regulators, and transmitters should not force their return currents through sensitive measurement connections. Automatically splitting analog and digital ground can create detours; grounding should follow the device’s layout guidance while preserving required isolation barriers.

Communication activity provides a useful prototype test. If readings change when a transmitter becomes active, its supply demand or coupled noise may be reaching the measurement circuit. Comparing idle and transmitting conditions helps expose behavior that remains hidden during a quiet bench test.

smart meter PCB

How Are Mains and Communication Circuits Isolated?

Isolation separates circuits that must operate at different electrical potentials. In one common arrangement, the metrology circuit operates at a mains-related potential, while an external communication interface sits across an isolation barrier.

The barrier must account for both data and power.

  • Data crosses through an isolation component, such as a digital isolator or an appropriate optocoupler, instead of a direct conductive signal connection.
  • The circuitry on the isolated side needs a suitable power source. A shared ground connection through its supply can defeat the intended isolation even when the data signal passes through an isolator.

The PCB must maintain the barrier around copper, component pads, connectors, and mounting features. Creepage is the distance along an insulating surface; clearance is the distance through air. Their required values depend on the insulation requirements and operating conditions, rather than one universal spacing for every smart meter.

Low logic voltage does not guarantee a safe voltage relative to earth. Similarly, a CT can isolate the current-sensing connection while other parts of the measurement circuit remain connected to mains. Programming cables, shields, and test fixtures must also preserve the intended separation.

How Do PLC and Wireless Modules Change the PCB Layout?

PLC requires a controlled connection to the power line; wireless communication requires a suitable antenna environment. This difference changes where components sit and which areas of the PCB need protection from interference.

Layout Feature Power-Line Communication (PLC) Wireless Communication
Signal connection Coupling network connects the communication circuit to the power wiring RF feed connects the radio to an integrated or external antenna
Space allocation Line interface, coupling components, filtering, and protection Module footprint, antenna area, and specified keepout
Sources of interference Line noise and interaction with the switching power supply Nearby switching circuits, unwanted coupling, and an unsuitable antenna environment
Product integration Line connection and coupling network affect communication performance Housing, terminals, shields, and nearby metal affect antenna performance

For wireless modules, antenna keepout and ground-plane requirements are different parts of the layout. An antenna may require a clear area while the rest of the module needs a ground plane. The module’s instructions determine where each applies.

Both communication methods can place changing loads on the power supply. Supply capacity and local decoupling must accommodate transmission without disturbing metrology. Testing the assembled meter in its intended enclosure also captures effects that are absent when a bare board operates on the bench.

What Determines the Layers and Copper Weight of an Energy Meter PCB?

Layer count follows the routing and reference-plane requirements. Copper weight follows the current carried by the PCB conductors, their permitted voltage drop, and temperature rise.

Layer count depends on how the circuits fit and connect.

A simpler meter may fit on two layers. Additional communication interfaces, dense routing, and limited board space may make four or more layers useful. Extra layers can provide routing space and reference planes, but they do not automatically improve accuracy: sensing paths, return currents, and isolation still need the correct arrangement.

Copper weight depends on the actual load-current path.

The meter’s rated current is not necessarily the current flowing through its PCB traces. A shunt, busbar, or terminal structure may carry the main load while the board carries only sensing signals and electronics supply currents. In another design, substantial load current may pass through PCB copper.

This distinction comes before specifying thicker copper. Where the board does carry significant current, conductor geometry and copper thickness affect resistance and heating. Thick copper also draws heat away from solder joints, so its electrical benefit must be accommodated by the assembly process.

How Does Smart Meter PCB Assembly Handle Precision and Power Components?

Assembly must preserve the electrical characteristics of the measurement parts while forming sound connections to larger power components. The two areas need different process controls.

Metering resistors and ICs need the specified parts and connections.

Two resistors can have the same nominal resistance but different tolerances and temperature coefficients. Substituting one for the other in a sensing network can change readings as temperature changes, even though the meter starts normally. Part-number control therefore matters alongside placement and solder-joint quality.

SMT assembly handles the metering IC, processor, and small passive components. Placement and soldering must preserve the intended connections, especially around fine-pitch pins and closely spaced sensing components.

Power terminals and large copper connections need sufficient soldering heat.

Large terminals and copper areas absorb heat differently from small SMT joints. Too little heat can leave poor wetting or insufficient solder fill; an unsuitable thermal process can damage nearby components. The soldering profile and method must suit the complete assembly.

Through-hole parts may use selective, wave, or controlled manual soldering. Assembly order must leave access to those joints and to inspection areas. Visual or optical inspection identifies assembly defects, while electrical and metering tests determine whether the completed circuit operates correctly.

How Are Smart Meter Boards Programmed, Calibrated, and Tested?

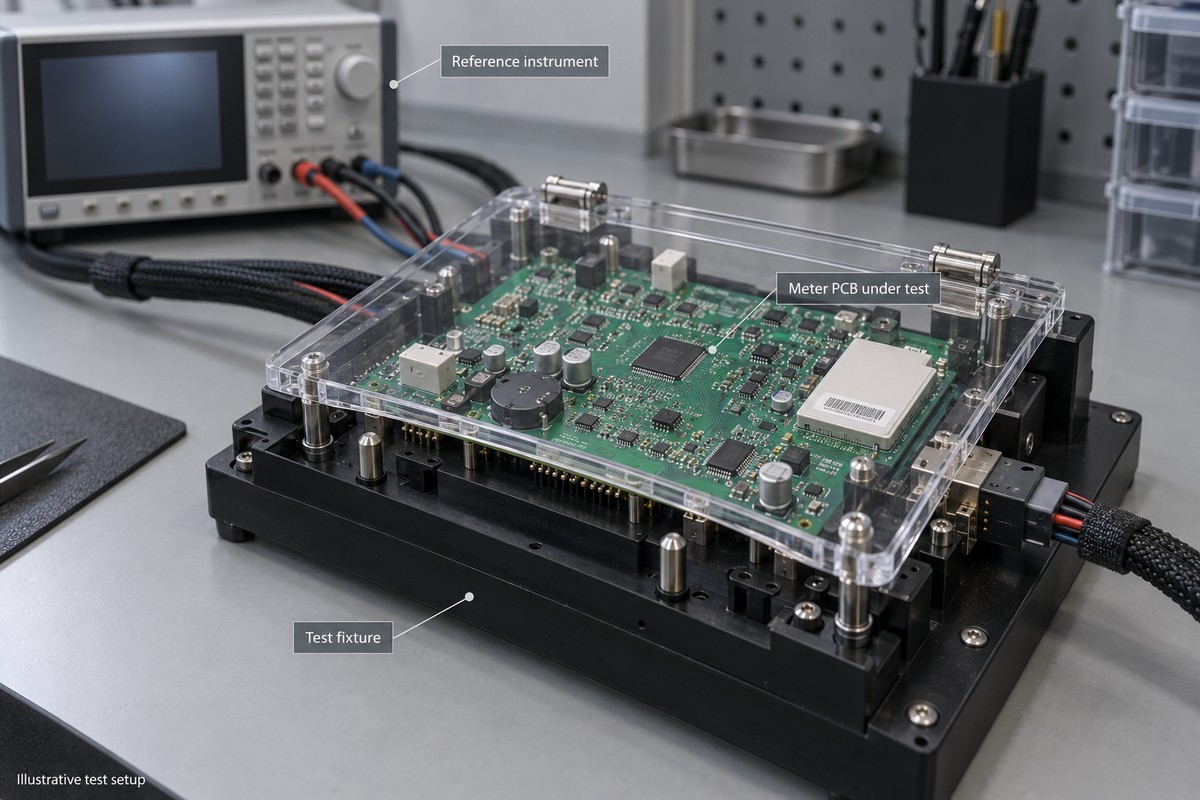
An assembled smart meter board is programmed with its intended firmware, calibrated against a reference, and then tested against defined acceptance limits. Calibration adjusts measurement behavior; verification measures the error that remains afterward.

  1. Load and verify the firmware and configuration. Programming installs the software and settings for the meter variant. Verification checks that the intended version and configuration were written successfully. Device identity is assigned where the product requires it.
  2. Compare the meter’s readings with a reference. The calibration setup applies known test conditions and compares the meter output with the reference result. Gain and phase corrections are calculated as required by the metering architecture; some designs also require offset correction. The resulting coefficients are stored for use during measurement.
  3. Measure performance after correction. Verification checks the remaining error at the current, voltage, and power-factor points defined for the product. Passing at the calibration point alone does not demonstrate accuracy across the operating range.
  4. Exercise the board’s other functions. Functional tests cover the power rails, display, memory, and supported communication interfaces. Power cycling checks whether required settings and calibration data are retained. Communication activity can also be included while measurement performance is observed.

The production record can associate each board’s identity with its firmware, calibration data, and test results. This makes a change in measurement performance easier to investigate across builds.

Production tests address the agreed board acceptance criteria. Complete meter certification also involves the applicable safety, EMC, environmental, and legal-metrology evaluations.

smart meter PCB

A reliable smart meter PCB build preserves the sensing connections, isolation boundaries, and component characteristics throughout manufacturing. EBest Circuit can support fabrication and assembly to your approved design, with testing agreed around the board’s actual functions. Contact sales@bestpcbs.com to discuss your prototype or production build.

You may also like

How to Choose the Right SMB Connector for Your RF Design
Wednesday, September 16th, 2026

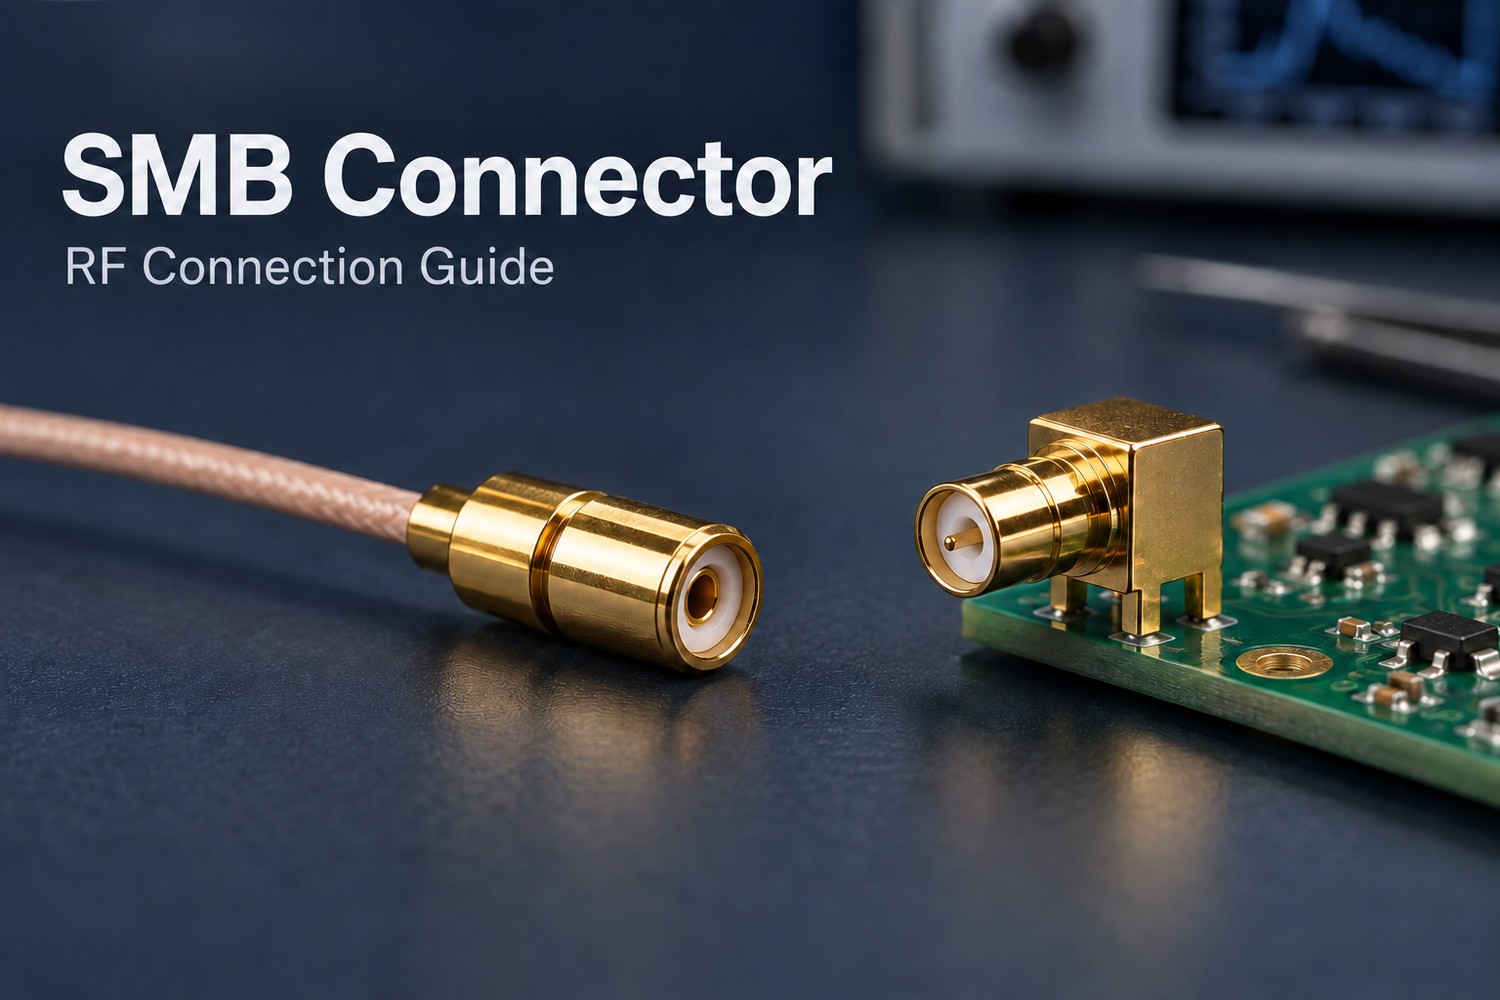
An SMB connector gives an RF design a compact, snap-on connection. Choosing the right version means matching the mating interface, system impedance, cable, and mounting arrangement. A connector that fits physically can still create an electrical mismatch or put unnecessary strain on the PCB.

EBest Circuit (Best Technology) combines PCB fabrication, component sourcing, and PCB assembly, including SMT and through-hole processes. This supports RF boards that need both a suitable connector footprint and a practical assembly process. Contact sales@bestpcbs.com to discuss your board and connector requirements.

SMB connector

What Is an SMB Connector?

An SMB connector, short for SubMiniature B, is a coaxial RF connector with snap-on coupling. It connects by pushing the mating halves together, without tightening a threaded nut.

Its coaxial structure has three main elements:

  • Center contact: carries the signal.
  • Dielectric: separates the conductors and helps establish impedance.
  • Outer conductor: provides the return path and shielding.

SMB is useful for compact internal RF links in communications equipment and instruments. Available versions include 50-ohm and 75-ohm interfaces, cable terminations, and PCB mounts; the family name alone does not specify their frequency rating.

How Do You Identify an SMB Plug and an SMB Jack?

In common standard SMB interfaces, the plug has a center socket and the jack has a center pin. This is easy to misread if you normally associate “plug” with a male pin.

SMB interfaceCenter contactMates with
PlugFemale socketCompatible SMB jack
JackMale pinCompatible SMB plug

Catalog labels such as “male” and “female” may describe the contact rather than the complete interface. Use the manufacturer’s mating drawing to resolve ambiguous descriptions.

Also keep interface gender and mounting style separate: a PCB mount is not a gender designation. For a replacement, match the interface first, then the impedance, footprint, and orientation.

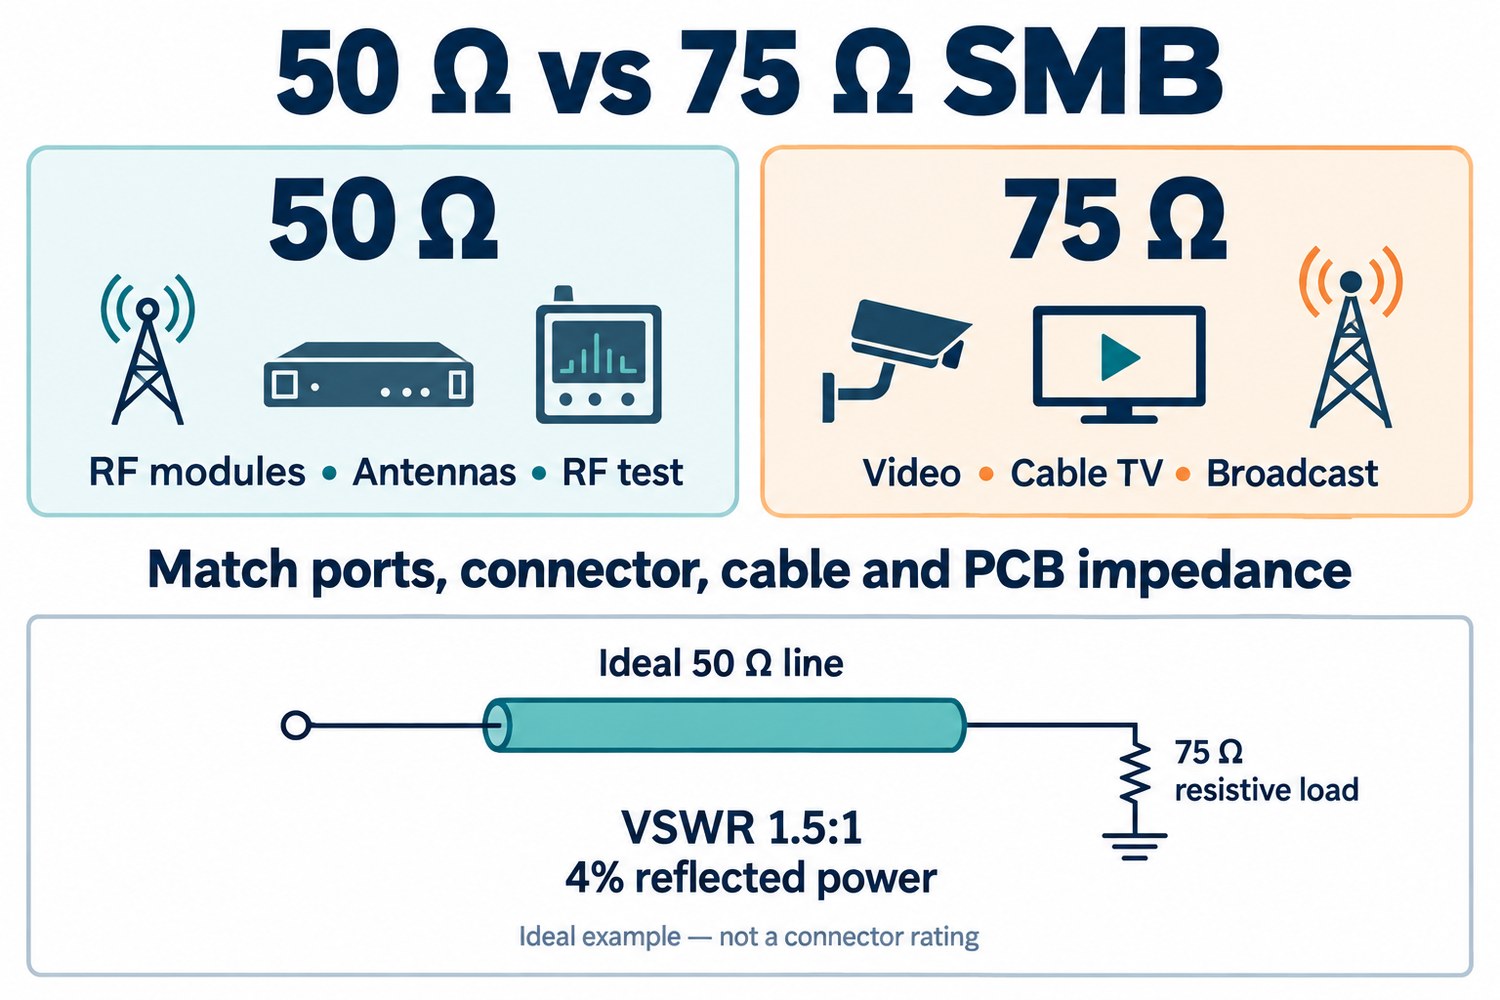
How Do 50-Ohm and 75-Ohm SMB Connectors Differ?

50-ohm and 75-ohm SMB connectors match different transmission-system impedances. The same distinction appears across several coaxial connector families:

ImpedanceCommon connector examplesTypical applications
50 ohmsSMA; 50-ohm BNC, N-Type, and SMBAntenna feeds, wireless modules, RF test equipment
75 ohmsF-Type; 75-ohm BNC and SMBCable television, video transmission, broadcast equipment

For SMB, conductor dimensions and dielectric geometry establish the impedance. Select the version that matches the equipment ports, coaxial cable, and PCB transmission line. Physical mating does not establish electrical compatibility.

A mismatch creates reflections and can raise VSWR. For example, an ideal 50-ohm line feeding a purely resistive 75-ohm load has a VSWR of 1.5:1, with 4% of incident power reflected. This illustrates the mismatch; it is not a universal rating for a 75-ohm SMB inserted into a 50-ohm assembly.

Actual results depend on frequency, connector transitions, cable length, and the PCB launch. Reflections can cause response ripple and reduce signal margin. Compare VSWR or return loss across the operating band: lower VSWR and higher return loss indicate a better match. Neither impedance is inherently superior.

SMB connector

SMA vs SMB Connector: Which Fits Your RF Connection?

SMB favors quick snap-on access; SMA provides a threaded connection. Choose around the required retention, service access, and operating frequency.

Design requirementSMBSMA
Connection methodPush to engage; pull the body to releaseThreaded coupling nut, tightened to specified torque
Installation clearanceRoom for axial movement and a secure gripRoom to turn the nut and use the required tool
Common fitCompact internal connections needing quick accessRF connections where threaded retention is preferred

Frequency capability belongs to the specific part. For example, Samtec lists SMB offerings with 50-ohm performance to 6 GHz and 75-ohm performance to 4 GHz. These figures do not apply to every SMB connector.

For vibration or moving cables, assess the connector’s retention specification and cable support. A coupling style alone does not establish environmental suitability.

Which SMB Cable Connector Fits Your Coaxial Cable?

Choose a connector approved for the exact cable construction, not just its impedance. RG316 is a common 50-ohm example; RG179 is used in 75-ohm assemblies. Their connector terminations are not automatically interchangeable.

Three details determine the fit:

  • Cable dimensions: the center conductor, dielectric, shield, and jacket must fit the contact and termination hardware.
  • Termination method: “crimp” may mean a crimped outer ferrule with a soldered center contact. Follow the specified stripping dimensions and tooling.
  • Cable exit: a right-angle body can reduce installed height; a straight body needs room for the cable’s bend radius.

Provide strain relief so cable pull is carried by the support structure rather than the termination or PCB solder joints.

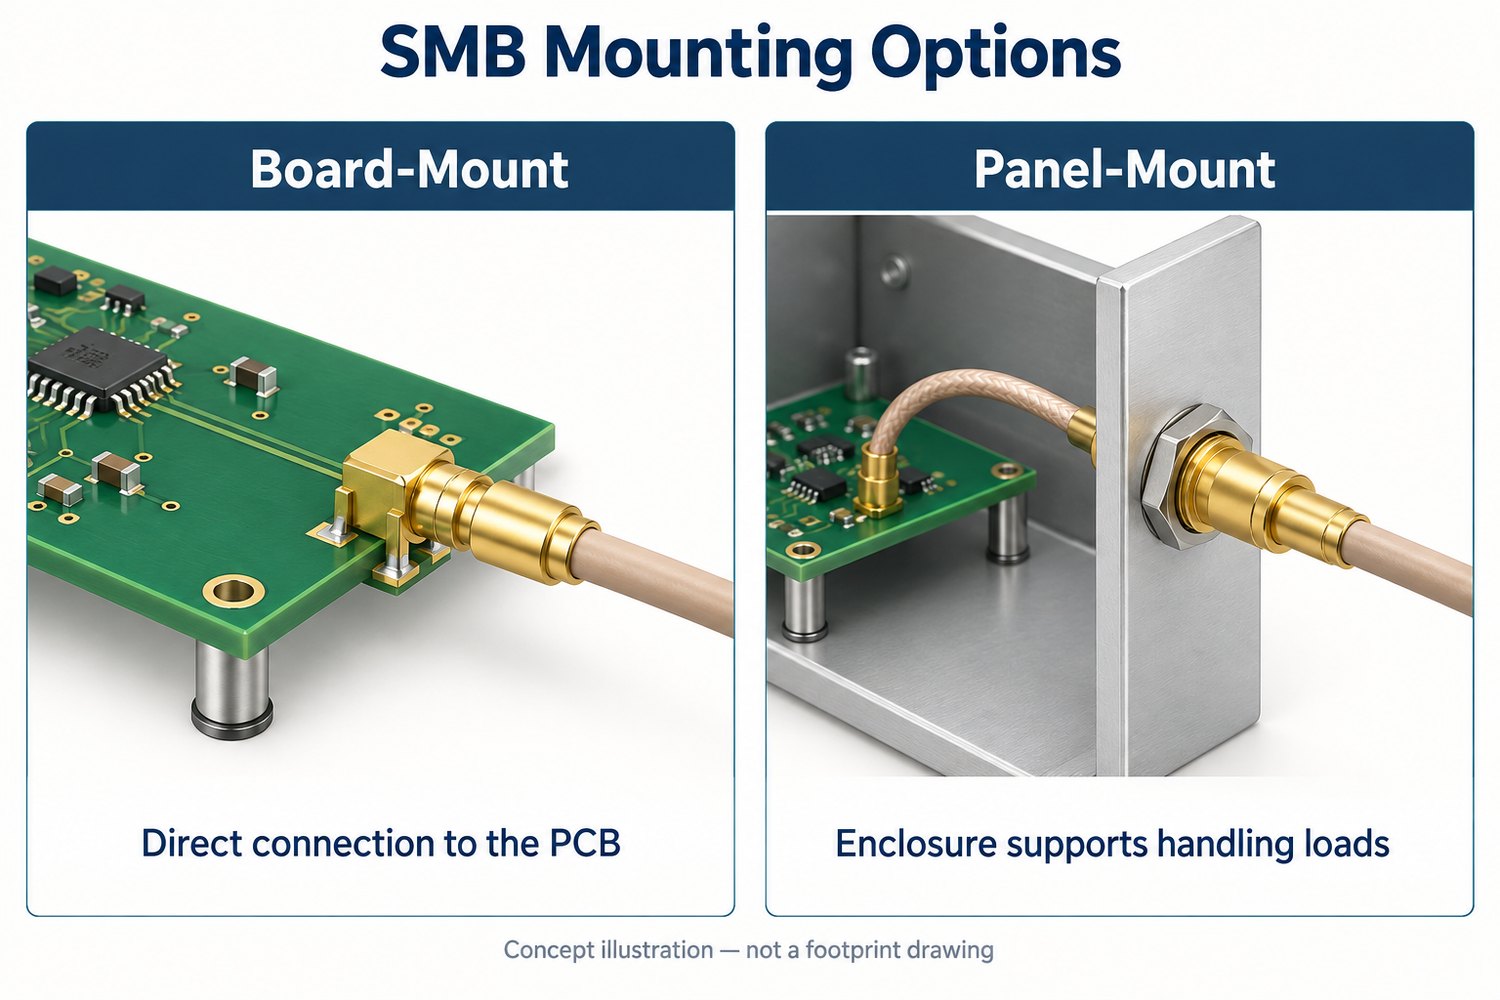
When Should You Choose a Board-Mount or Panel-Mount SMB Connector?

Use board mounting for a direct PCB connection and panel mounting when the enclosure should support the accessible interface. Some connectors combine PCB termination with bulkhead mounting.

  • Board-mount: suits a direct cable-to-board RF path. The manufacturer’s footprint, ground connections, and signal transition matter because the connector-to-trace junction is part of the RF circuit.
  • Panel-mount: suits an externally accessed port. A properly supported bulkhead transfers plugging and cable-handling forces into the enclosure.

Check the assembled geometry: board-to-panel distance, panel thickness, connector orientation, and finger clearance. Compatible SMB mating faces do not guarantee identical PCB footprints.

For the board-side details, see our guide to SMB PCB fabrication and assembly.

SMB connector

How Do You Connect and Disconnect an SMB Connector?

Push and pull along the mating axis while holding the connector body. Standard snap-on SMB interfaces do not screw together like SMA.

  1. Inspect: look for debris, bent contacts, or shell damage. Follow the equipment’s RF power-down instructions.
  2. Align: bring both halves onto the same axis before applying pressure.
  3. Seat: push steadily until fully engaged. Stop if resistance feels abnormal.
  4. Release: support the fixed connector and pull the mating body straight back.

Do not pull on the cable or lever the connector against the PCB. Where access is restricted, provide more clearance or use a manufacturer-approved removal tool.

FAQs About SMB Connectors

Are SMB, Mini-SMB, and SSMB interchangeable?

No interchangeability should be assumed. They are separately specified interface families; similar names and snap-on coupling do not guarantee matching dimensions. Use the manufacturer’s mating information.

Are SMB connectors waterproof?

Not by designation. An exposed connection needs an explicit protection rating covering the connector, termination, and intended assembled condition.

Does an SMB-to-SMA adapter match 75 ohms to 50 ohms?

A basic interface adapter does not automatically transform impedance. If the circuit requires impedance matching, use an appropriate matching device or network.

Does the connector rating establish the cable assembly’s frequency performance?

No. Cable length and loss, both connectors, and terminations affect the finished assembly. Use assembly-level insertion-loss and return-loss specifications for the operating band.

What causes a loose SMB connection?

Possible causes include incomplete engagement, incompatible mating parts, worn retention features, or a loose mount. Identify the cause and replace damaged parts; do not squeeze the shell or bend contacts to tighten the fit.

Planning an RF board with an SMB connector? Send your PCB files, BOM with the connector part number, and required quantity to sales@bestpcbs.com. EBest Circuit can support fabrication, sourcing, and assembly around your selected components.

You may also like

How Do You Choose an Aluminum Frame PCB Stencil?
Tuesday, September 15th, 2026

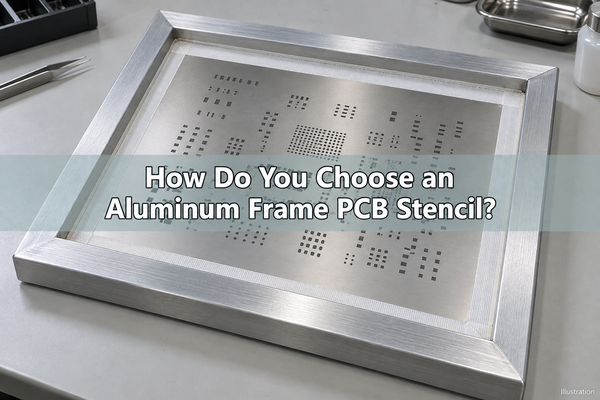
An aluminum frame PCB stencil holds a patterned metal foil under tension so solder paste can be printed onto PCB pads before component placement. The aluminum is the support frame, not normally the printing foil. At EBest Circuit (Best Technology), we supply custom SMT stencils and PCB assembly support. For your project, the useful starting points are printer compatibility, aperture geometry, foil thickness and the final panel layout.

Illustration of an aluminum frame PCB stencil with a mesh border and stainless steel foil

What Is an Aluminum Frame PCB Stencil?

A framed PCB stencil combines three working parts: a rigid frame, a tensioned mesh border and a thin metal foil containing openings that correspond to the solder-paste pattern. The squeegee moves paste across the foil; the openings control where paste reaches the board. After separation, the paste deposits remain on the pads.

The distinction between frame material and PCB stencil material matters when ordering. Aluminum provides a lightweight, rigid support. Stainless steel is commonly used for the PCB stencil foil because it can be fabricated with fine openings and withstand repeated printing and cleaning. A steel foil does not turn the finished circuit board into an aluminum PCB.

A PCB framed stencil is a complete mounted tool, whereas a stencil blank is an unpatterned starting material. If you need a working circuit board stencil, specify the aperture file and mounting arrangement, not just the frame dimensions.

Framed vs Frameless Stencil: Which Suits Your Production?

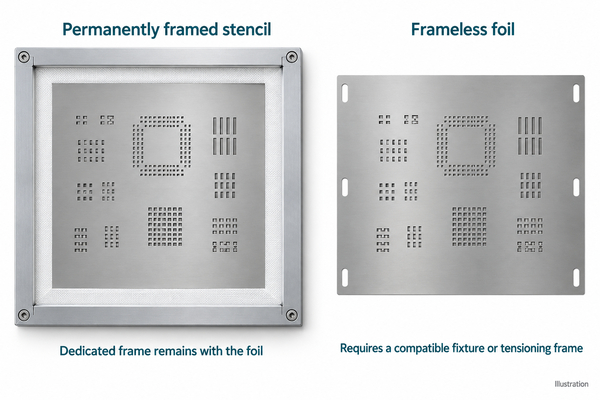
A permanently framed tool is useful for repeat builds on compatible equipment. A frameless foil can suit either a manual fixture or a reusable tensioning system, but those are different setups. Frameless does not automatically mean unsuitable for production.

Illustration comparing a permanently framed stencil with a frameless foil requiring compatible mounting
Option Best fit What to check
Permanently framed stencil Recurring assemblies with a dedicated tool Printer fit, stored-frame space, mesh and bond condition
Frameless foil in a reusable frame Multiple designs sharing compatible tensioning hardware Foil mounting interface, tensioning procedure and changeover time
Unframed foil in a manual fixture Low-volume builds and development work Flat support, registration and repeatability of the fixture

For a frameless PCB stencil printer, confirm the foil attachment system before ordering. A foil made for one tensioning system may not fit another. Prototype SMT stencils should therefore be selected around the intended printing process, not around a fixed prototype-versus-production label.

What Frame Size Fits Your Stencil Printer?

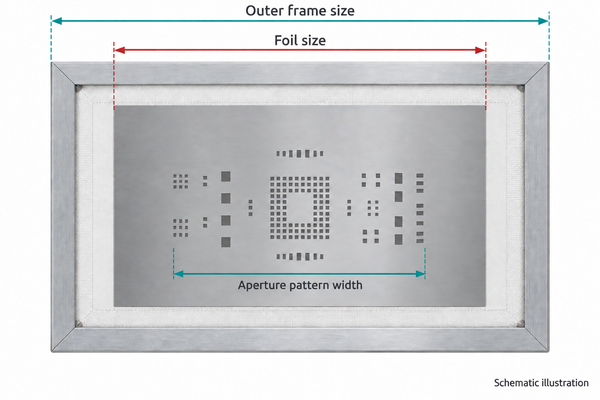
There is no single PCB stencil standard size that fits every printer. The outer frame must fit the machine clamps, while the usable printing area must accommodate the complete panel and squeegee travel. Frame profile, thickness, mounting direction and underside-cleaning clearance also affect compatibility.

Schematic distinguishing outer frame size, foil size and aperture pattern width

An SMT stencil frame drawing should distinguish the outer frame size, foil size and aperture-pattern envelope. The actual printable area is further limited by bonding margins and the printer mechanism; it is not simply the entire foil. Send the printer model or approved mounting drawing instead of ordering a frame from PCB length and width alone.

A PCB stencil holder or PCB stencil jig must support registration without bending the foil or board. For our FR4 printed circuit boards, use the released panel drawing, including rails, orientation and fiducials, when preparing the stencil. Changing the panel after cutting can make an otherwise accurate stencil unusable.

How to Choose PCB Stencil Thickness?

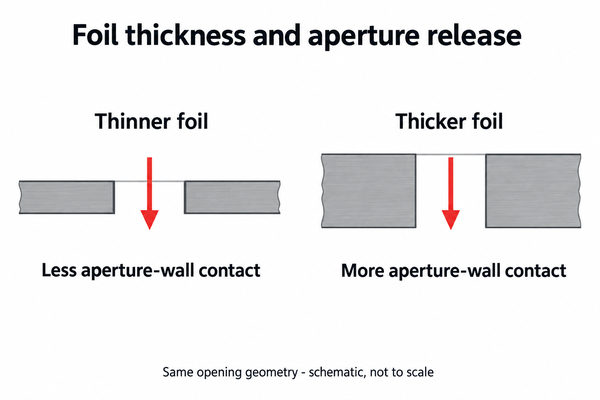
Choose thickness from the paste-volume requirements of the component mix and the release behavior of the smallest openings. A thicker foil provides more theoretical paste volume for the same aperture, but also increases the wall area that the paste must release from. More thickness is not automatically better.

Our custom SMT stencil options cover a foil-thickness range of 0.10-0.60 mm across different stencil applications, subject to engineering review. This capability range is not a recommended thickness range for every fine-pitch SMT board. We also offer step-up and step-down stencil options where different areas need different deposit volumes.

For mixed fine-pitch ICs and larger terminals, evaluate a uniform foil first, then consider local thickness changes if the requirements conflict. Step locations need clearance from nearby apertures and suitable squeegee access. Component pitch alone is not enough to select PCB stencil thickness.

How Does SMT Stencil Aperture Design Affect Paste Release?

SMT stencil aperture design determines both deposit geometry and release conditions. For a rectangular opening with length L, width W and foil thickness t, area ratio is LW / [2t(L + W)]. Aspect ratio is W/t when W is the smaller opening dimension. These describe different geometric relationships.

Schematic showing greater aperture-wall contact with thicker stencil foil for the same opening
Illustrative opening Foil thickness Area ratio Theoretical aperture volume
0.30 × 0.60 mm 0.10 mm 1.00 0.018 mm³
0.30 × 0.60 mm 0.15 mm 0.67 0.027 mm³

These calculated values illustrate geometry, not a guaranteed process window or measured deposit. Actual transfer depends on paste, aperture-wall condition, separation settings and board support. A PCB stencil thickness calculator cannot replace a print trial on the intended assembly.

For large thermal pads, multiple smaller windows may help distribute paste more appropriately than one large opening. For small pads, excessive aperture reduction can make release harder. PCB stencil design should use the component manufacturer’s land-pattern guidance, target deposit and assembly process together; a universal reduction percentage is not suitable for every footprint.

Which Fiducials and Panel Details Must Match?

PCB stencil fiducials let the printer align the foil pattern to the board. Their locations, optical contrast and marking method must suit the vision system. A fiducial is not necessarily an open hole: etching, filling or other marking arrangements depend on the printer and stencil specification.

For double-sided assemblies, identify top and bottom paste files explicitly and confirm viewing direction. Do not mirror a file merely because it is named bottom. The manufacturing output convention and assembly orientation must agree. When both sides share one foil, the printer’s working area, orientation and separation between patterns need approval.

Keep the PCB paste layer, panel drawing and assembly revision synchronized. The solder-mask layer is not a substitute for the paste layer: mask openings expose board features, while paste apertures define deposits for assembly.

How Is a Laser Cut PCB Stencil Made?

A laser cut PCB stencil is produced by cutting the approved aperture pattern into metal foil, applying the specified finishing operations and mounting the foil to its support system. In a permanently framed construction, the foil and mesh bond must maintain the required tension and flatness during use.

Our PCB stencil service includes laser-cut, etched, framed and unframed constructions, as well as electropolishing options. For a laser cut SMT stencil, electropolishing can improve aperture-wall condition, but it does not correct the wrong aperture geometry, foil thickness or panel file. The finishing requirement belongs in the order specification.

Before release, agree on the features that need verification: aperture dimensions and positions, foil thickness, image orientation, frame compatibility, bond condition and tension where specified. For fine-feature work, clarify the measurement method and acceptance criteria rather than assuming the word precision defines them.

How to Use a PCB Stencil?

The basic sequence is alignment, printing, controlled separation and deposit inspection. For a new framed tool, a short first-article print check is more useful than assuming that successful clamping proves process readiness.

  1. Confirm the stencil revision, print side and matching PCB panel.
  2. Support the board and align the apertures to the pads using the printer’s specified registration method.
  3. Apply compatible solder paste and use the established squeegee and separation settings for the assembly.
  4. Inspect deposit alignment, bridging, missing paste and consistency before placing components.
  5. Adjust the process or aperture design from the observed defect, rather than compensating for every problem with more pressure.

SMT solder paste stencils are printing tools, not reflow fixtures. The stencil is removed before placement and reflow. Through our PCB assembly services, we support SMT, through-hole and mixed assemblies; discuss stencil supply together with your assembly files when you need a coordinated PCB and PCBA order.

How Should Framed Stencils Be Cleaned and Stored?

Use a cleaning method compatible with the solder paste, foil, mesh and bonding adhesive. Residue inside an aperture can reduce the next deposit, while contamination beneath the foil can contribute to smearing. Follow the applicable cleaning-equipment and chemistry instructions, and protect personnel according to the relevant safety information.

Do not scrape fine openings with tools that can alter their geometry. After cleaning, check for blocked apertures, dents, corrosion, lifted bonding and mesh damage. A visibly clean foil is not automatically a flat, tensioned tool.

Store each tool by design, side and revision in a protected SMT stencil rack or equivalent support. Prevent contact with the active foil area. Reuse depends on condition and validated printing performance, not a universal number of print cycles. A replacement foil must also match the original mounting system.

What Affects the Price of a Framed PCB Stencil?

Price depends on frame size, foil specification, aperture complexity, finishing, step features, inspection requirements and delivery arrangements. A low tool price can be poor value if it requires a new holder, cannot fit the printer or has to be remade after a panel revision.

Compare quotations against the same drawing and scope. Ask whether the price includes the aluminum frame, patterned foil, mounting, specified finishing and inspection. For repeat orders, confirm whether an existing frame can be reused and whether that service is actually included.

For suitable stencil orders, we can provide turnaround as fast as one working day. Availability depends on the design, finishing and order review; production time is separate from transport time. Tell us the required arrival date so that the quotation can address both.

What Files Do We Need for Your Custom Stencil?

For a custom aluminum frame PCB stencil, send the released paste-layer data and final panel information first. We accept Gerber and supported PCB/CAD design files. A PDF can explain dimensions and notes, but a drawing alone may not contain the complete aperture geometry needed for manufacture.

Input Include
Design identity Part number, revision, top/bottom side and units
Aperture data Paste Gerber or supported design files, approved modifications and critical features
Panel and alignment Final panel drawing, rails, fiducials and print orientation
Printer interface Machine model, outer frame dimensions, frame profile and clamping requirements
Foil and finishing Requested thickness, step regions, surface treatment and inspection criteria
Order scope Quantity, stencil-only or PCB/PCBA supply, destination and required arrival date

If the thickness or aperture treatment is not yet defined, identify the fine-pitch devices and larger solder-volume features for review instead of guessing a specification. Send your aluminum frame PCB stencil requirements to sales@bestpcbs.com. Our team can discuss the stencil construction and manufacturing scope with you before quotation.

You may also like

How Do You Read Electrical Circuit Diagram Symbols?
Tuesday, September 15th, 2026

Electrical circuit diagram symbols represent components and their electrical connections, not the physical shape of a finished board. To read them, identify each symbol, follow its connected nets, then check values, polarity and pin numbers. For a PCB project, those details must remain consistent from the schematic through the component list, footprint and assembly drawing.

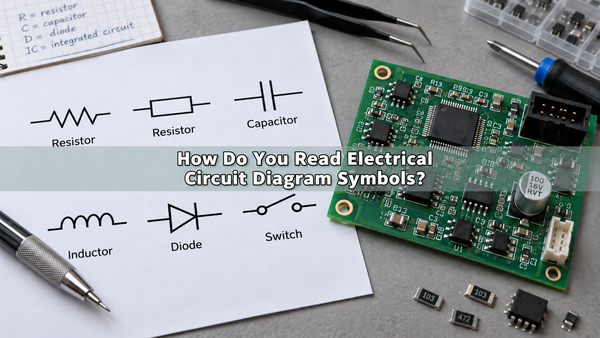
Electrical circuit diagram symbols on a reference sheet beside a PCB, conceptual illustration

What Are Electrical Symbols in Circuit Diagrams?

Electrical symbols are graphical shorthand for functions such as resistance, energy storage, switching and amplification. A circuit diagram uses electrical symbols to represent components and lines to show the intended connections between their terminals. A resistor drawing identifies a resistor; its label and linked part record specify which resistor belongs on the board.

Electrical symbols and electronic symbols overlap. A battery, switch or connector can appear in both a machine control schematic and a small electronic assembly. The difference is the system being described, not a completely separate alphabet. This guide concentrates on electronic circuit symbols used in PCB-related drawings rather than building floor-plan notation.

Common Circuit Symbols and Functions

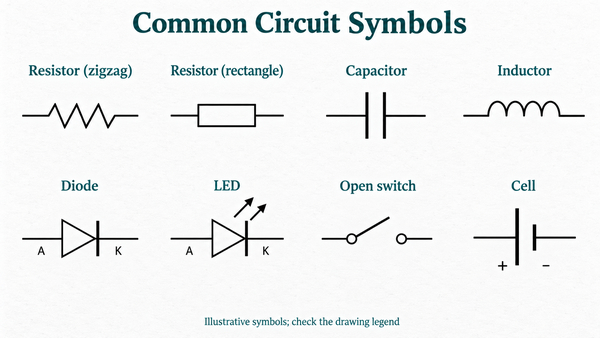
The most useful starting point is a circuit symbols chart that pairs the drawing with its function and the detail you must verify. The illustration shows basic electrical circuit diagram symbols; the table explains how to interpret them without treating the shape as a complete component specification. Together they form an electrical symbols chart with reading checks, not a list of interchangeable parts.

Original electrical symbols chart showing resistors, capacitor, inductor, diode, LED, switch and cell
Component Typical drawing cue Function and reading check
Resistor Zigzag or rectangle Limits current or establishes voltage ratios. Read resistance, tolerance and power rating.
Capacitor Two plates; polarized versions may show + Stores charge and supports filtering or coupling. Check capacitance, voltage rating and polarity.
Inductor Coil; some versions include core markings Stores magnetic energy. Check inductance, current rating and the specified part.
Diode / LED Diode with cathode bar; LED adds outward arrows Diode conduction is directional. LED arrows represent emitted light, not extra terminals.
Cell / battery Unequal parallel lines; repeated pairs for a battery Provides DC energy. The longer line indicates the positive side; voltage requires a label.
Switch Contact points and movable contact Makes, breaks or changes a connection. Identify the pole, throw and shown state.
Fuse Small inline fuse element, convention-dependent Overcurrent protection. Read current, voltage and time-current characteristics.
Transistor / IC Device-specific symbol or pin-labelled block Switches, amplifies or processes signals. Confirm pin names, numbers and supply connections.

These schematic symbols of electronic components describe electrical roles. Ratings and package dimensions belong in the component data and bill of materials (BOM); they cannot be inferred from how large the symbol is drawn.

What Is the Symbol for Electric Wire?

A straight line represents an electrical connection. A filled junction dot normally joins intersecting wires; crossing lines without a dot normally remain separate in modern electronic schematics. Older drawings may use a curved crossover or different junction conventions, so check the legend before tracing an unfamiliar design.

Wires that share a net label can be connected even when no continuous line runs across the page. In hierarchical designs, local, global and sheet-level labels have different scopes. Matching visible text alone does not prove that two labels on different sheets form one net.

Illustrative connected and unconnected wire crossings, matching net labels and ground reference symbols

A bus groups named signals; it is not a copper short between every signal inside it. A no-connect marker on an unused pin also differs from a junction dot. When checking an electrical schematic drawing, use net highlighting or the connection list to resolve an ambiguous intersection instead of guessing from a low-resolution image.

How Do Power, Battery and Ground Symbols Differ?

Power symbols identify sources or supply nets, while a ground symbol identifies a reference or grounding connection. Neither the position of a symbol nor the word GND alone establishes a physical connection to protective earth.

What is the symbol for battery?

The battery circuit symbol commonly uses alternating long and short parallel lines. One pair represents a cell; multiple pairs represent a battery. The number of drawn pairs is not a reliable cell-count specification, and the symbol does not establish voltage or chemistry. Read the stated supply value and battery part information.

What are symbols for AC and DC current?

A sine-wave mark commonly indicates AC, while a solid line above a dashed line indicates DC in equipment notation. Circuit source symbols may instead show a sine wave, +/− signs or a directional arrow inside a circle. The letter I is the usual current symbol in equations; it is not a component or a substitute for an AC/DC rating.

Earth, chassis and circuit-reference symbols serve different purposes. Circuit reference is the node used for voltage measurements; chassis refers to the frame or enclosure; protective earth is part of a safety connection. They may be connected by a deliberate design, but must not be assumed interchangeable. Separate AGND and DGND labels likewise require an intentional connection strategy, not an automatic split in the PCB ground plane.

How Do You Read Resistor, Capacitor and Inductor Symbols?

Read the symbol first, then the component value and its surrounding connections. Passive components with identical drawings can perform very different jobs depending on where they sit in the circuit.

Resistor symbols and adjustment arrows

The resistor schematic symbol can be a zigzag or rectangle. A diagonal adjustment arrow indicates a variable element; a potentiometer normally has two end terminals and a third wiper terminal. A fixed resistor connected from a digital input to a supply is a pull-up, while the same component in series with an LED limits current.

For readers asking what schematic symbol represents a current limiter, there is no single answer for every circuit. A series resistor can limit current, but regulated current limiting may use an IC, transistor and sense resistor. The circuit function must be established from the connections and ratings.

Capacitor and magnetic-component details

A non-polarized capacitor symbol uses two plates. Polarized versions may add a + sign and sometimes a curved plate; the explicit polarity marking and component datasheet take priority. A ceramic capacitor is not made polarized simply by the orientation of its label.

An inductor symbol is commonly a coil. Added core markings distinguish some symbol variants; two coupled windings indicate a transformer. Dots on coupled windings describe relative winding polarity, not junctions connecting the windings. A symbol alone does not specify saturation current, insulation rating or the complete magnetic construction.
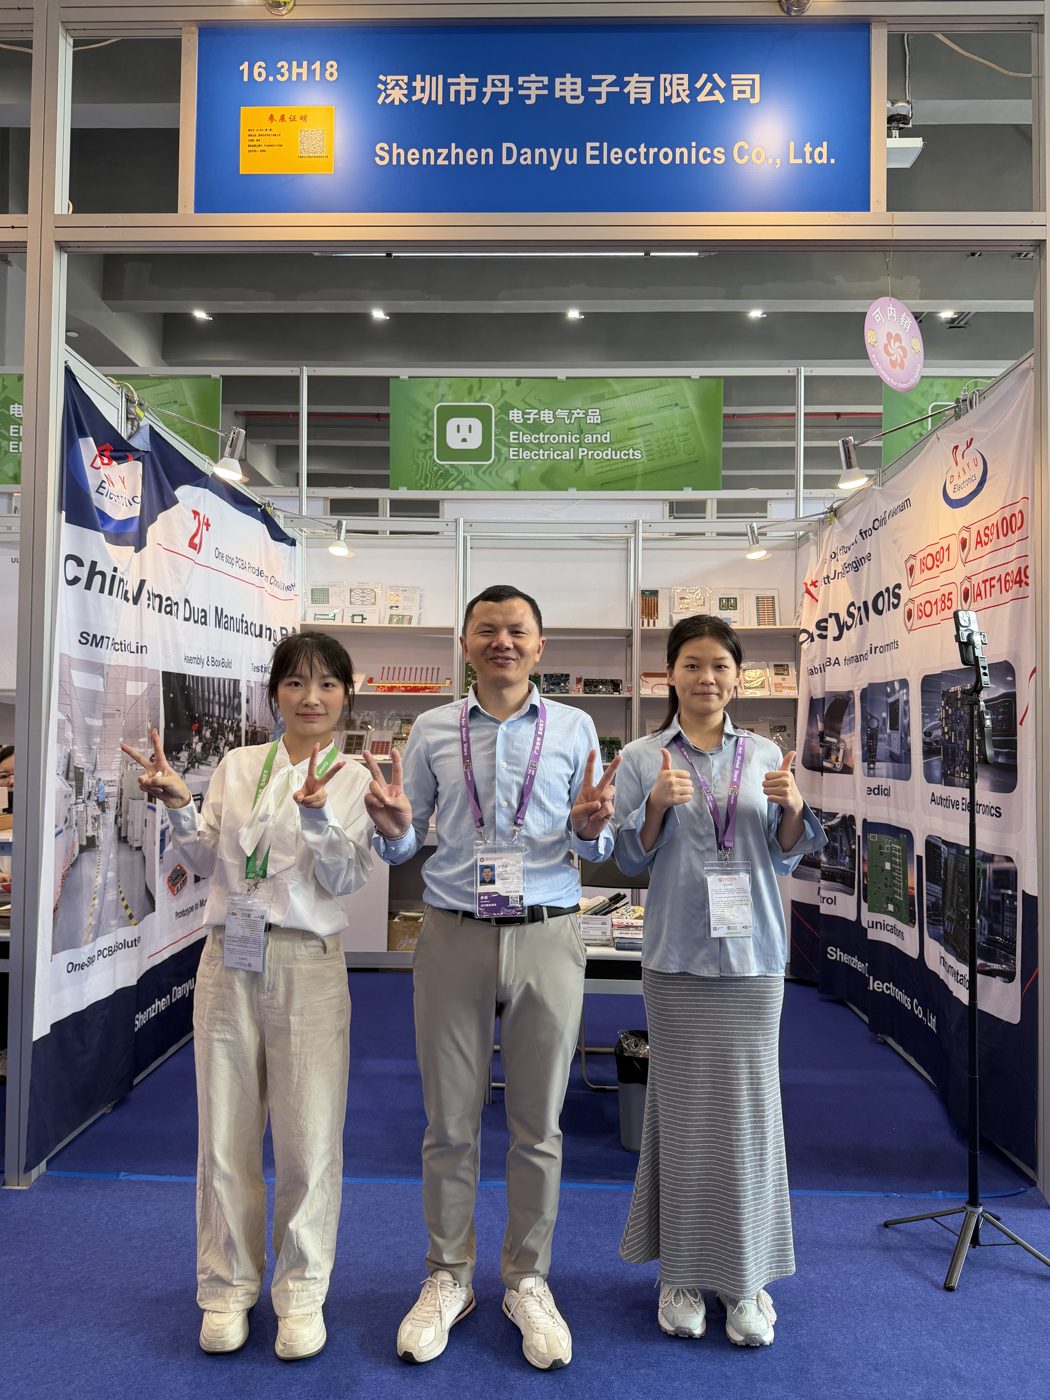
How Do Diode and LED Symbols Show Polarity?

The diode’s bar identifies the cathode, commonly labelled K; the other terminal is the anode, A. Conventional forward current passes from anode to cathode when the device is appropriately forward biased. Rotating the symbol changes its position on the page, not the terminal identities.

The LED symbol adds arrows pointing away from the diode to indicate emitted light. A photodiode uses arrows pointing toward it. Zener and Schottky devices use modified cathode markings, so a generic diode sketch is not enough to identify the correct BOM part.

Before PCB assembly, match the schematic polarity to the footprint pad numbering and the component drawing. Do not assume every library assigns pin 1 to the same terminal. Our rectifier diode guide covers the additional voltage, current and recovery checks needed for rectification circuits.

How Do Switch, Relay and Protection Symbols Work?

A switch symbol shows which contacts connect in the illustrated state. SPST has one switched path; SPDT connects one common terminal to either of two alternatives. Pole and throw describe the contact arrangement, not the number of decorative lines or package pins.

What is the symbol for a single pole switch?

For a simple SPST switch, two contact points and a movable line show an open or closed path. Normally open and normally closed refer to a defined normal condition, commonly an unactuated switch or de-energized relay. Read any drawing note that specifies a different state.

In electrical control circuit diagram symbols, a relay coil and its contacts may be drawn far apart and linked by a common reference. Their physical separation on the schematic does not mean they are separate devices. A limit switch adds an actuation function; the associated mechanical state still needs to be understood.

A fuse and a circuit breaker symbol both concern protection, but they do not describe interchangeable parts. A fuse is normally replaced after operation; a breaker may be reset after the fault is addressed. Contact symbols do not establish safe working voltage, interrupting capacity or regulatory approval.

How Are Transistors, Logic Gates and IC Pins Represented?

Active-device symbols identify functions and terminal relationships. The pin names and part-specific pinout are what connect the drawing to the real package.

On a bipolar transistor, B, C and E identify base, collector and emitter. The emitter arrow points outward for NPN and inward for PNP. A MOSFET uses gate, drain and source, and its symbol may show a body diode. Its appearance is not permission to swap source and drain.

Logic circuit symbols distinguish AND, OR, inversion and other functions. A small output bubble indicates inversion; a triangle without that bubble may be a buffer. An operational amplifier also has a triangular body, but its + and − inputs and supply requirements identify a different function. Those input signs are not the amplifier’s power pins.

Large ICs are often rectangular blocks with named and numbered pins. One physical package may be split into several schematic units, including a separate power unit. For fine-pitch devices on HDI PCBs, accurate pin-to-pad mapping must precede escape routing: the logical symbol does not determine the required via structure.

Why Do IEC and ANSI-Style Schematic Symbols Look Different?

Different symbol conventions can represent the same electrical function. The familiar resistor rectangle is associated with IEC-style drawings, while the zigzag is common in ANSI/IEEE-style drawings. Neither shape alone changes resistance or selects a regional component.

IEC 60617 concerns graphical symbols for electrotechnical diagrams. CAD libraries and legacy documents may use different variants, particularly for logic, grounding and switches. Follow the drawing’s stated convention and legend rather than expecting every electrical schematic symbols chart to look identical.

For an unfamiliar symbol, first check its reference, terminal names and linked part number, then compare it with the library definition. A copied image can omit a polarity mark, inversion bubble or connection dot that changes the interpretation.

What Do R1, C1, Values and Pin Numbers Mean?

A reference designator identifies one component instance; a value describes an electrical property; a pin number maps a terminal to the package. Mixing these three kinds of circuit notation is a common cause of schematic-to-BOM errors.

Marking Meaning What to confirm
R1, C1, L1, D1 Common references for resistor, capacitor, inductor and diode The same reference identifies the same part in the BOM and PCB files.
U1, Q1, J1 Common references for an IC, transistor and connector Project conventions vary; check the library and assembly drawing.
4k7 / 4R7 4.7 kΩ / 4.7 Ω Do not confuse a multiplier with a reference prefix.
100 nF / 0.1 µF The same capacitance value Voltage, dielectric and tolerance still need specification.
Pin 1 / A / K Package number or functional terminal name Check the selected symbol-to-footprint mapping; do not infer numbering from left/right position.
DNP / DNI Do not populate / do not install Ensure assembly variants agree across BOM, drawing and placement data.

A value is not a complete purchasing description. Two 10 kΩ resistors can differ in package, tolerance and power rating. For multi-unit devices, make sure the separate units still resolve to one physical part and that all supply pins are accounted for.

How to Read Circuit Diagrams?

Trace a complete path from the supply through the load and back to the return, checking the state of each component along the way. This gives the individual symbols a circuit-level meaning.

Illustrative closed-switch LED circuit with 5 V supply, 1 kilohm resistor and approximately 3 mA under stated assumptions
  1. Find the +5 V supply and 0 V return. The source is connected at the two labelled terminals.
  2. Follow S1. It is shown closed, so the series path continues through R1.
  3. Read R1 as 1 kΩ. It limits the current rather than setting the LED voltage directly.
  4. Identify D1’s anode and cathode. The cathode bar is on the return side.
  5. Estimate current using the stated assumptions: I = (5 V − 2 V) / 1,000 Ω = 3 mA.
  6. Check what changes when S1 opens: the series path is broken and the ideal steady-state LED current becomes zero.

The 2 V LED forward drop is an illustrative assumption, not a value for every LED. Actual current depends on the selected LED, supply tolerance, resistor tolerance and temperature. The resistor dissipates approximately 9 mW in this example; its selected rating still needs suitable operating margin.

To draw a circuit diagram, place symbols from the appropriate library, connect their electrical pins, add values and annotate references. Run electrical rules checking (ERC), then inspect the circuit function. ERC can find certain connection conflicts but cannot prove that the design will perform as intended.

How Do Schematic Symbols Become a Manufacturable PCB?

A schematic defines logical connectivity; a PCB layout defines physical pads, tracks, vias and placement. A wiring diagram instead emphasizes connections between terminals, cables or assemblies. Wiring diagram symbols can overlap with schematic notation, but the documents answer different questions.

For FR4 printed circuit boards, the net information must be translated into copper geometry with suitable spacing, current capacity and return paths. A neat electrical schematic diagram does not, by itself, establish board thickness, layer stack-up or trace dimensions.

At EBest Circuit (Best Technology), we provide PCB assembly services for SMT, through-hole and mixed assemblies. Our assembly capability includes 01005 SMD components and BGA pitch down to 0.25 mm, subject to review of the actual package, PCB and process requirements. Clear polarity, pin mapping and assembly-variant information are particularly important for small components and dense packages.

For a fabrication and assembly quotation, send your current Gerber and drill files, BOM with manufacturer part numbers, pick-and-place data and assembly drawing. Include the schematic and any special test or polarity requirements so we can discuss ambiguities against the same design revision. A schematic screenshot alone is not a complete manufacturing package.

Reading electrical circuit diagram symbols is the first step; consistent component and manufacturing data keep that meaning intact on the finished board. Send your project files to sales@bestpcbs.com for PCB and assembly review.

You may also like

What Is a Rectifier Diode and How Does It Work?
Tuesday, September 15th, 2026

A rectifier diode is a semiconductor component that conducts mainly in one direction and blocks reverse current within its voltage rating. It is used to turn AC into a unidirectional, pulsating output. On a PCB, its performance depends on more than the part number: current, switching speed, polarity, copper paths and cooling must work together.

Rectifier diode concept illustration showing axial and surface-mount packages on a PCB

What Is a Rectifier Diode?

A rectifier diode is a diode selected for power rectification rather than primarily for processing small signals. Its two terminals are the anode and cathode. An individual diode is a component; a diode rectifier can be a complete circuit containing several devices, or an integrated bridge package.

In a PCB power supply, rectification is only one stage. Filtering reduces ripple, and a regulator controls the output voltage. A diode alone does not provide a smooth, regulated supply or electrical isolation.

How Does a Rectifier Diode Work?

The rectifier diode function follows its bias condition. With sufficient forward bias, conventional current flows from anode to cathode. Reverse bias greatly reduces that current, but leakage remains; exceeding the device’s reverse-voltage capability can damage it.

What does a rectifier diode do when the input alternates? In a simple series circuit, it passes one half-cycle and blocks the other. Arranging multiple devices into a full-wave circuit lets both input half-cycles deliver current through the load in the same direction.

Forward voltage is not a fixed 0.7 V. It changes with current, temperature and diode technology. A PN device also takes time to remove stored charge when switching from conduction to blocking, so a diode that suits a low-frequency supply may be unsuitable in a switching converter.

What Does the Rectifier Diode Symbol Mean?

The rectifier diode symbol identifies the anode and cathode; the straight bar marks the cathode. On many axial rectifiers, a band on the body identifies that same terminal. Match the symbol, package drawing and PCB footprint before assigning placement orientation. The rectifier diode diagram below relates the physical band to the two terminals.

Rectifier diode diagram relating the axial cathode band to anode and cathode terminals

A rectifier diode number such as 1N4007 identifies an electrical device family, not a complete footprint specification. Supplier suffixes can change packaging and lead details. For SMD parts, confirm the manufacturer marking drawing rather than relying on a stripe convention alone. A readable polarity mark on the assembly drawing helps prevent a correct component being fitted backward.

How Do Half-Wave and Full-Wave Rectifier Circuits Differ?

A half-wave circuit uses one input half-cycle; a full-wave circuit uses both. In a single-phase rectifier diode circuit, the common full-wave choices are a four-diode bridge or a two-diode circuit with a center-tapped transformer secondary.

CircuitDiodes and sourceEffect on the load
Half-waveOne diode with an AC sourceOne pulse per input cycle; larger gaps between charging pulses
Full-wave bridgeFour diodes; no center tap requiredTwo pulses per cycle; two diodes conduct in series in each current path
Center-tapped full-waveTwo diodes and a center-tapped secondaryTwo pulses per cycle; each half-secondary conducts on alternate half-cycles
Conceptual comparison of AC input, half-wave output and full-wave output without a smoothing capacitor

How Many Diodes Are Used in a Bridge Rectifier?

A single-phase diode bridge rectifier uses four diodes. Its two alternating current paths each contain two conducting devices. This full wave bridge rectifier arrangement is convenient, but its two forward drops can be significant on a low-voltage rail.

In half wave rectifier diode selection, account for the interval in which the load receives no input energy. In full wave rectifier diode selection, consider which winding and diode pair carry current at each instant. A bridge rectifier diode must handle the charging pulses as well as the reverse-blocking interval.

A smoothing capacitor changes the current waveform: the diodes recharge it in pulses near the AC peaks. Diode peak current can therefore be much higher than the average load current. Ripple and inrush must be considered together, not solved by choosing a larger capacitor alone.

Which Rectifier Diode Types Suit Your Circuit?

Rectifier diode types differ in switching behavior and losses. Start with the circuit frequency and reverse voltage, then compare forward loss, leakage and package cooling.

TechnologyTypical fitMain selection trade-off
Standard silicon PN rectifierLow-frequency AC rectificationLow cost, but recovery may be too slow for a switching stage
Fast or ultrafast PN rectifierSwitching power conversionRecovery charge and softness must be weighed against forward loss
Silicon Schottky rectifierLow-voltage rails and fast switchingLow forward loss can be useful; reverse leakage rises with temperature
SiC Schottky rectifierHigher-voltage, high-frequency conversionAssess switching loss, conduction loss, cost and thermal design together

Rectifier Diode vs Diode: What Is the Difference?

A rectifier is one use of a diode, not a separate opposite category. A small-signal switching diode is optimized for a different combination of current, capacitance and speed. A silicon rectifier diode cannot be replaced safely just because another diode has the same outline.

Rectifier Diode vs Schottky Diode

A Schottky rectifier diode is itself a rectifier. Compared with a conventional PN part, a silicon Schottky device often offers lower forward voltage and avoids minority-carrier storage recovery, but capacitive switching current still exists. Verify leakage at the expected temperature rather than assuming the lowest forward drop always produces the coolest design.

How Do You Distinguish Between Zener Diode and Rectifier Diode Functions?

A Zener diode is designed to operate in controlled reverse breakdown for voltage-reference or clamping tasks. A conventional rectifier normally works in forward conduction and reverse blocking. Swapping these roles without checking ratings can destroy the device or stop the circuit working.

Is 1N4007 a Rectifier Diode?

Yes. The 1N4007 rectifier diode is a common general-purpose silicon PN rectifier. A representative DO-41 version has a 1,000 V repetitive peak reverse-voltage rating and a 1 A average forward-current rating, with the current rating tied to specified mounting and temperature conditions.

For this DO-41 example, the 1 A condition uses 9.5 mm leads at 75°C ambient; maximum forward voltage is 1.1 V at 1 A under the stated electrical test conditions. These are device limits, not a promise that any small PCB can deliver a continuous 1 A DC output. Check the exact manufacturer’s datasheet, derating curve and rectifier circuit before substitution.

Its familiar part number does not make it the default for high-frequency rectification. Standard recovery, package dissipation and surge loading may matter more than its high reverse-voltage rating.

How Do You Select Rectifier Diode Ratings?

Select the device against the actual circuit waveform and temperature, not just the nominal supply voltage. The key ratings answer different questions.

ParameterWhat to check
VRRMWorst repetitive reverse voltage, including circuit topology and expected transients; do not compare only with AC RMS voltage
IF(AV)Average forward current under the specified cooling, waveform and temperature conditions
IFSMNon-repetitive surge capability for the stated waveform and duration; not a continuous operating rating
VFForward loss at operating current and junction temperature
IRReverse leakage at operating voltage and temperature
trr and QrrReverse recovery time and charge under comparable test conditions
Tj and thermal resistanceAllowable junction temperature and the actual path from device to board, enclosure or heatsink

For a simple conduction-loss estimate, average the instantaneous product of diode voltage and current over time. Using VF × average current can be a first approximation when VF is represented appropriately; it does not include recovery or reverse-leakage losses. High-frequency designs need those additional terms.

Rectifier diode price also depends on package, qualification, voltage class and order quantity. A lower component cost is not a saving if it requires more cooling, a larger board or a different assembly process.

How Should Rectifier Diodes Be Laid Out on a PCB?

Give the rectifier a short current path, adequate copper and an unambiguous footprint. The board must carry pulsed current and remove heat without compromising insulation spacing.

For many control and low-power supply designs, FR4 printed circuit boards provide the required routing and mechanical support. Size conductors for the actual current waveform, copper thickness, allowable temperature rise and surrounding layout. Minimum fabrication line width is not a power-trace recommendation.

Conceptual PCB rectifier layout highlighting wide copper paths, polarity markings and separation from heat-sensitive capacitors
  • Keep the bridge-to-reservoir-capacitor charging loop compact, including its return path.
  • Use the specified land pattern and thermal-pad connection; do not add copper that bridges different electrical nodes.
  • Separate hot rectifiers from electrolytic capacitors and temperature-sensitive circuitry where practical.
  • Determine clearance and creepage from working voltage, environment and the applicable product requirements; do not use one spacing for every supply.
  • Make the cathode orientation consistent across schematic, silkscreen, assembly drawing and placement data.

For higher-current paths, our heavy copper PCBs provide 4–10 oz copper options, subject to review of the complete design. Thicker copper can help current distribution and heat spreading, but it does not remove the diode’s junction-temperature limit. Wider conductors, pad geometry and soldering heat demand must be considered together.

How Do You Test a Rectifier Diode?

A multimeter’s diode mode can reveal a gross short or open circuit, but it does not prove the device will meet its high-voltage, current or switching ratings. Disconnect power, safely discharge stored energy and verify that no voltage remains before testing. Mains-connected supplies require qualified handling.

  1. With the isolated diode in forward bias, connect the red probe to the anode and the black probe to the cathode.
  2. Read the forward-voltage indication and compare it with the expected device technology and the meter’s test conditions.
  3. Reverse the probes. A normal reverse-blocking result usually appears as an over-range indication.
  4. If the result is ambiguous in circuit, isolate a terminal using an appropriate rework procedure; parallel paths can mislead the reading.

A near-zero reading both ways can indicate a short. Over-range both ways can indicate an open diode, but poor contact or insufficient meter test voltage can produce a similar result. Board-level diagnosis should also check solder joints, polarity and the surrounding circuit. A successful diode-mode reading does not replace a powered functional test under controlled conditions.

What Happens When a Diode Shorts in a Bridge Rectifier?

A shorted diode can create a heavy fault-current path during part of the AC cycle, potentially operating a fuse or damaging other components. Disconnect the supply and investigate the bridge and surrounding circuit before replacing parts; do not keep energizing the board to see whether the fault clears.

How Do We Build PCBs for Rectifier Circuits?

At EBest Circuit (Best Technology), we manufacture the PCB and assemble the specified components into your power-conversion circuit. Our PCB assembly services cover SMT, through-hole and mixed assembly, so an axial rectifier, an SMD diode and larger connectors can be incorporated into one board build.

We check incoming components against your BOM and support inspection and functional testing as part of the agreed assembly scope. Provide the exact diode part number, board files, polarity information and operating requirements so we can review the build consistently. Component selection remains tied to the approved design; we do not substitute a familiar diode number solely because the footprint fits.

For your next rectifier diode PCB project, send the fabrication files, BOM and assembly drawings to sales@bestpcbs.com. We can help connect the required copper construction, component mounting and assembly requirements in one manufacturing review.

You may also like

What Does J-STD-003 Reveal About PCB Solderability?
Friday, September 11th, 2026

J-STD-003 addresses the solderability of bare printed circuit boards: whether the exposed surfaces intended for soldering can be wetted by molten solder. For your PCB project, that matters before components reach the assembly line. At EBest Circuit (Best Technology), we connect PCB fabrication and assembly support so that the board finish, component layout and soldering process are considered together.

J-STD-003 PCB solderability concept illustration showing exposed pads and plated-through holes

What Is J-STD-003?

IPC J-STD-003 (also written IPC J STD 003 or J STD 003) is the solderability test standard for printed boards. Its subject is the board’s exposed conductors, attachment lands and plated-through holes, rather than component leads or completed solder joints.

Solderability testing helps separate a surface-wetting problem from an assembly-process problem. A satisfactory bare-board result does not prove that every joint will form correctly during production: solder paste deposition, component placement and the thermal profile remain separate parts of assembly quality.

Why Can a PCB Look Clean but Solder Poorly?

A clean-looking pad is not necessarily a readily wettable pad. Thin oxidation or contamination can interfere with the solder-to-metal interface without producing an obvious defect in an ordinary board photograph.

On our FR4 printed circuit boards, the solderable features include both surface-mount pads and connection points for through-hole parts. If solder withdraws from a pad, the resulting connection can be incomplete even though the copper circuit passes an electrical continuity test. Continuity and wettability answer different questions.

Appearance also depends on the solder alloy. Lead-free solder does not necessarily spread or look like tin-lead solder, so a comparison based only on shininess can be misleading. The important distinction is whether the intended metal surface has been wetted under the applicable test conditions.

Which Solderability Test Methods Are Used?

J-STD-003D includes visual evaluation methods and wetting-force measurement. The method must suit the board features being assessed.

Method familyMain evaluation
Edge dipWetting of exposed surface conductors
Surface-mount simulationWetting of surface-mount lands
Wave solder or solder floatSolderability of plated-through-hole features
Wetting balanceWetting behavior recorded as force over time

For a board carrying both fine-pitch components and connectors, a surface-pad observation cannot answer every question about the holes. Likewise, a test on an unrelated reference board cannot establish the condition of your production lot. Representative material and the agreed evaluation method are essential to a useful result.

What Does a Wetting Balance Test Measure?

A wetting balance test records the force acting on a specimen as it contacts molten solder. The force-time response shows how wetting develops, adding information that a photograph taken after cooling cannot provide.

Conceptual wetting balance test with a PCB coupon, solder bath and illustrative force-time curve

The response reflects surface tension, buoyancy and the developing solder meniscus. Test temperature, alloy, flux and specimen geometry affect the signal; curves obtained under different conditions are not automatically comparable. The illustration shows the measurement principle, not a measured result or a pass/fail limit.

For a difficult-to-solder pad, this measurement can help investigate delayed or weak wetting. It does not identify the root cause by itself, and it does not replace examination of the finish or the actual assembly process.

How Do Nonwetting and Dewetting Differ?

Nonwetting means solder has not formed the intended wetted interface. Dewetting describes solder withdrawing after initially covering an area, leaving an uneven coating. Both can reduce useful solder coverage, but they describe different behavior.

ObservationWhat it suggestsWhat it does not prove
Solder beads beside an uncovered padPossible nonwetting of that surfaceThat the PCB finish is the sole cause
Irregular solder islands after coverage recedesPossible dewettingA specific contamination source without further analysis
Smooth-looking solder on only part of the featureIncomplete coverage still needs evaluationAcceptance based on appearance alone

For an assembly defect, the PCB pad and the component termination should be distinguished. A board can have satisfactory solderability while a component lead has a separate surface problem. Adding more heat or flux without identifying the affected interface can damage the assembly rather than resolve the cause.

How Does PCB Surface Finish Affect Solderability?

The surface finish protects exposed copper and establishes the surface presented to the soldering process. ENIG, OSP, immersion silver, immersion tin and HASL use different protection systems, so the finish name alone cannot describe every assembly constraint.

Conceptual comparison of an ENIG plated pad and an OSP protected copper pad before soldering
FinishRelevance to assemblyProject consideration
ENIGFlat nickel-gold finish for component landsFinish integrity and the planned soldering sequence
OSPOrganic protection over copper without a raised solder coatingHandling, storage and cumulative thermal exposure
Immersion silver or tinThin metallic protection on exposed copperPackaging and finish-specific assembly conditions
HASL or lead-free HASLSolder coating on exposed featuresPad planarity and alloy compatibility

For our HDI boards, fine-pitch pad geometry makes surface planarity and solder-paste deposition particularly relevant. A readily wettable finish cannot compensate for a stencil opening that delivers too little paste. Our finish options include ENIG, ENEPIG, OSP, immersion silver, immersion tin and lead-free HASL; we match the available construction to your board and assembly requirements.

Can Storage and Repeated Heating Change the Result?

Yes. The condition of a solderable surface can change between fabrication and assembly. Packaging, handling and thermal exposure therefore matter alongside the original finish selection.

A double-sided assembly may expose the second-side pads to heat before they are soldered. A later selective-soldering operation adds another thermal stage. These histories differ from soldering a fresh, unheated specimen, and their effect depends on the finish and process.

For boards held in storage, the production date alone is not a complete description of their condition. Whether the original packaging stayed intact and whether surfaces were exposed to contamination are also relevant. Baking should not be treated as a universal way to restore solderability: a moisture-removal step cannot simply reverse oxidation or damaged surface chemistry.

Is J-STD-003 Class 3 the Same as Coating Durability?

No. J-STD-003 Class 3 concerns the product classification; coating durability is a separate rating. A higher product class does not automatically specify an aging treatment.

In J-STD-003D, coating-durability notation differs between Pb-containing and Pb-free finishes. Category 2 or Category 3 terminology must not be exchanged blindly with the lettered categories for another finish system. Your specified revision and finish determine the applicable requirements.

What Is the J-STD-003 Latest Revision?

The J STD 003 latest revision listed when this article was checked in September 2026 is J-STD-003D. Older J-STD-003B and J-STD-003C references still appear in drawings and search results; they should not be treated as interchangeable editions.

If an existing design calls for an earlier revision, changing its acceptance basis is an engineering decision, not just a document-name update. We work from the agreed fabrication requirements rather than silently substituting a newer edition.

How Is J-STD-003 Different from J-STD-002 and J-STD-001?

The main difference is what is being evaluated: the bare board, the component connection surface, or the assembled soldered connection. The related standards are complementary, not substitutes.

StandardPrimary subject
J-STD-003Printed-board solderability
J-STD-002Solderability of component leads, terminations and related connection surfaces
J-STD-001Requirements for soldered electrical and electronic assemblies
J-STD-004Soldering flux requirements
J-STD-005 / J-STD-006Solder paste / electronic-grade solder alloys and related forms

For example, a connector joint joins a board barrel to a component pin. Evaluating the barrel does not establish the pin’s solderability, while evaluating both surfaces still leaves the production soldering process to be controlled. This is why one bare-board test result cannot stand in for complete assembly acceptance.

How Do We Connect Bare-Board Quality with PCB Assembly?

We provide PCB fabrication and PCB assembly services, including SMT, through-hole and mixed assembly. This lets us consider the solderable board surface together with the components and the planned assembly sequence.

Concept illustration showing the same PCB layout before and after surface-mount and through-hole assembly

Our FR4 manufacturing capability extends to 32 layers, with the final construction subject to engineering review. For a multilayer controller with dense surface-mount parts and through-hole connectors, the board stack-up, pad finish and thermal demands all affect how fabrication and assembly fit together. We review these requirements as a connected PCB project, not as an isolated finish choice.

Discuss your J-STD-003 requirement with our engineering team at sales@bestpcbs.com. We can review the fabrication drawing, surface finish and assembly plan, and confirm the applicable project requirements before production. Any dedicated test method, sampling arrangement or report requirement must be agreed for that project.
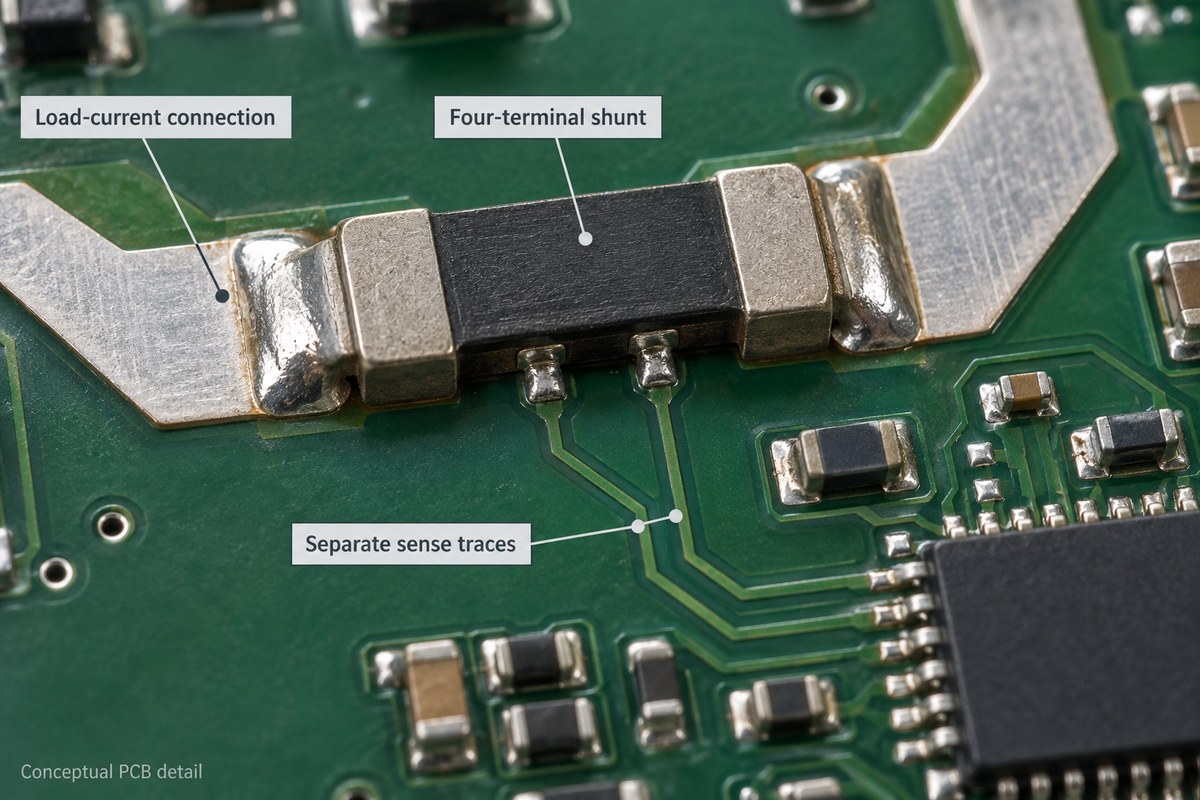
You may also like