

PCB manufacturing PCB manufacturing
Home > Blog

Pull Up vs Pull Down Resistor: How to Choose the Right One

August 19th, 2026

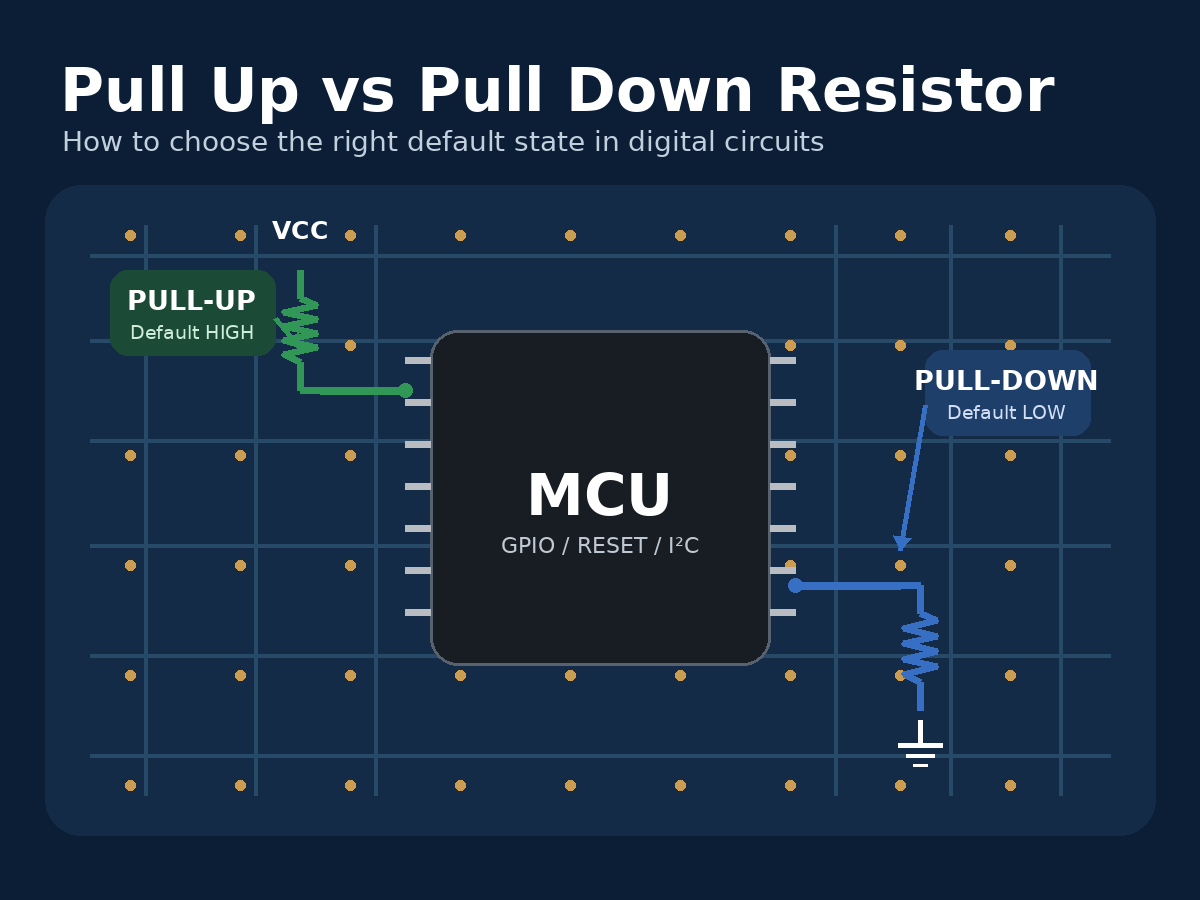
A pull up vs pull down resistor comparison comes down to one basic decision: what logic state should a signal have when no device is actively driving it? A pull-up resistor keeps the signal HIGH by connecting it to the positive supply through resistance, while a pull-down resistor keeps it LOW by connecting it to ground. Both prevent a high-impedance digital input from sitting at an undefined voltage.

The difference is simple, but choosing the right arrangement becomes more important in real circuits involving MCU GPIO, reset and enable pins, sensors, open-drain outputs, I²C buses, and power-up sequencing. This guide explains how pull-up and pull-down resistors work, when to use each type, how to select a suitable resistor value, and what engineers should check before a design moves from schematic to PCB production.
pull up vs pull down resistor

Pull Up vs Pull Down Resistor: What Is the Difference?

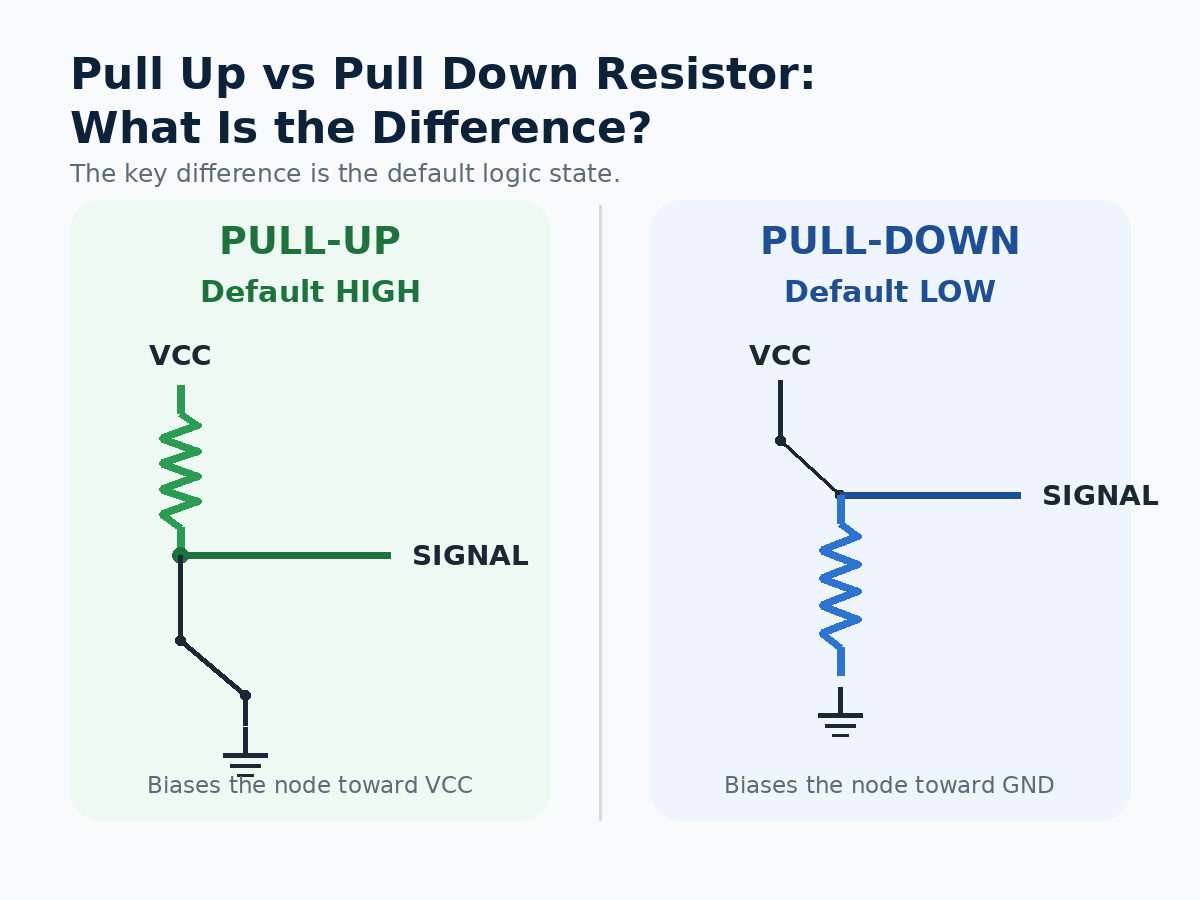
The main difference between pull-up and pull-down resistors is the default logic state they establish.

A pull-up resistor connects the signal to VCC, so an undriven input normally reads HIGH. A pull-down resistor connects the signal to ground, so the same type of input normally reads LOW.

Design PointPull-Up ResistorPull-Down Resistor
Resistor connectionSignal to VCCSignal to GND
Default logic stateHIGHLOW
Typical active stateLOWHIGH
Common switch connectionSignal to GNDSignal to VCC
Common usesOpen-drain signals, reset lines, interrupts, MCU inputsEnable pins, gate control, default-low inputs
Logic behaviorOften active-lowOften active-high

Neither method is inherently better. The correct choice depends on what the circuit should do when the switch, controller, or external signal is inactive.

A useful first rule is:

Default HIGH → use a pull-up.
Default LOW → use a pull-down.

For open-drain or open-collector signals, a pull-up is normally required because the output can actively pull the line LOW but cannot actively drive it HIGH.
pull up vs pull down resistor

How Do Pull-Up and Pull-Down Resistors Work?

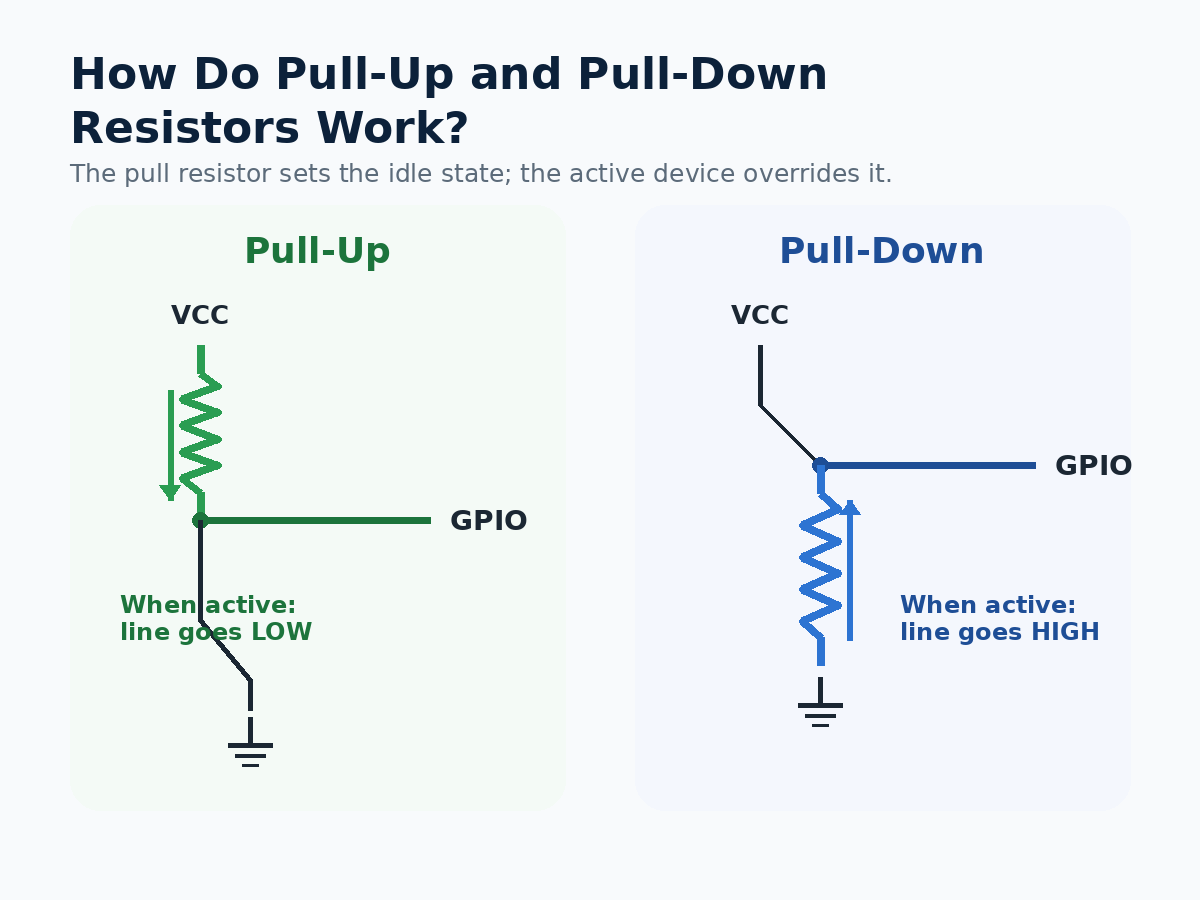
Pull-up and pull-down resistors provide a weak connection to one power rail while allowing another device to override that state.

Pull-up resistor circuit

A pull up resistor circuit typically connects:

VCC → resistor → signal node

A switch, transistor, or open-drain output can then connect the signal node to ground.

When nothing drives the line, the resistor brings the node toward VCC. When the signal is pulled to ground, the resistor limits the current between VCC and GND.

For example, with a 3.3 V supply and a 10 kΩ resistor:

I = V / R = 3.3 / 10,000 ≈ 0.33 mA

Pull-down circuit

A pull down circuit reverses the arrangement:

Signal node → resistor → GND

An external source can then drive the node toward VCC. When that source is removed, the resistor brings the signal back toward ground.

The resistor therefore does two jobs: it establishes a known idle voltage and limits current when another device drives the line in the opposite direction.

This is why simply connecting a signal directly to VCC or GND is not equivalent to using a pull resistor. A direct connection could create excessive current when another device attempts to drive the opposite state.
pull up vs pull down resistor

Why Are Pull-Up and Pull-Down Resistors Needed?

Digital inputs often have very high input impedance. If an input is disconnected and has no pull-up or pull-down path, it can become a floating input.

A floating node may respond to leakage current, residual charge, nearby switching signals, EMI, or capacitive coupling. The voltage can move between valid HIGH and LOW thresholds instead of remaining at a predictable level.

That can create behavior such as:

  • an MCU input changing state without a valid command;
  • a reset or enable pin activating unexpectedly;
  • a MOSFET control node entering an unintended state;
  • intermittent sensor or digital-interface behavior;
  • unstable operation during startup or controller reset.

The startup condition deserves particular attention in production electronics. Firmware does not configure every GPIO immediately when power is applied. An external pull resistor can establish the required state before firmware runs.

For example, an enable pin that must remain inactive during power-up may use a pull-down resistor even if the microcontroller later controls that signal directly.

Pull resistors are therefore not merely “logic accessories.” They help define circuit behavior during the moments when no active driver is in control.

When Should You Use a Pull-Up or Pull-Down Resistor?

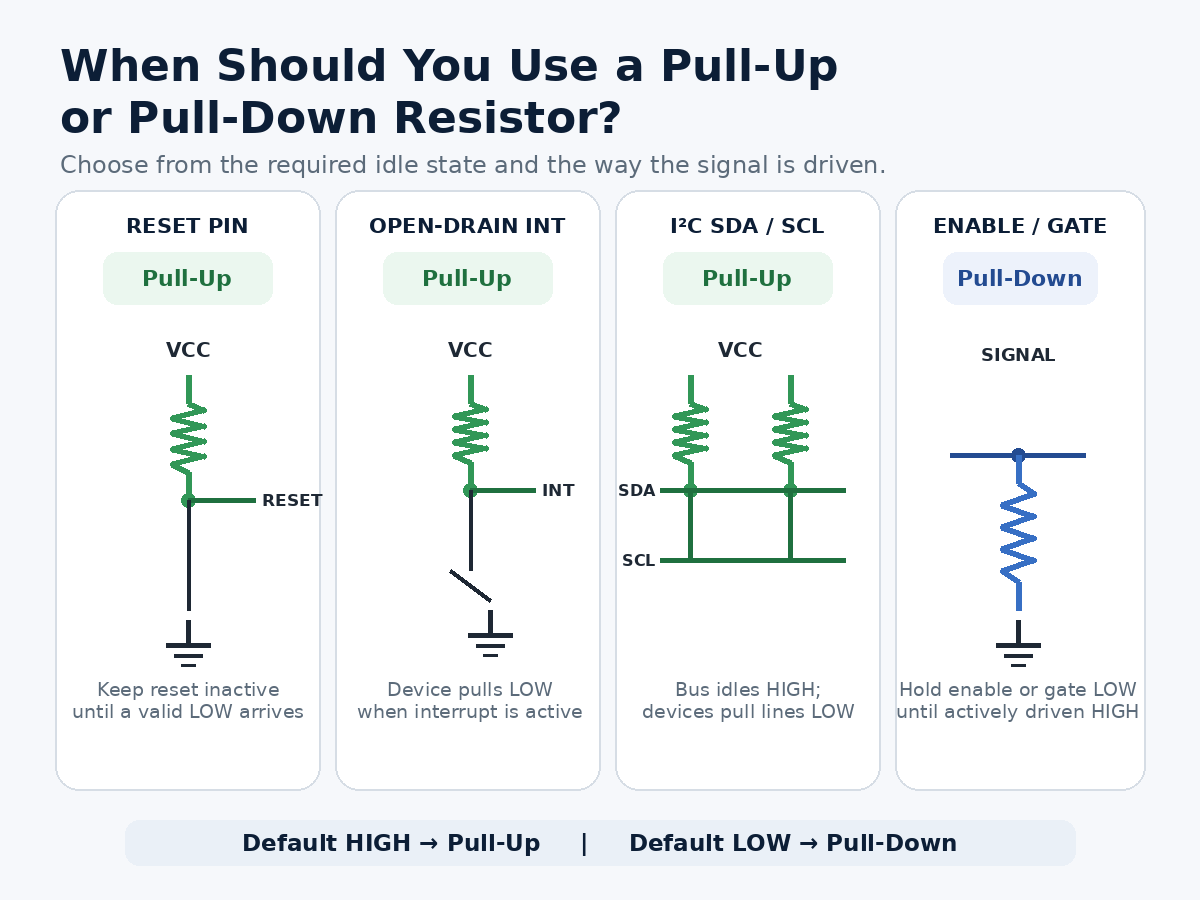
The easiest way to choose between them is to start with the required idle state and then check how the active device drives the signal.

Use a pull-up resistor when:

  • the signal should default HIGH;
  • a switch or transistor pulls the line toward ground;
  • the signal is active-low;
  • an open-drain or open-collector output is used;
  • reset, interrupt, or chip-select lines should remain HIGH when inactive;
  • a communication interface requires a passive HIGH state.

Use a pull-down resistor when:

  • the signal should default LOW;
  • an external device drives the node toward VCC;
  • an enable pin must remain disabled during startup;
  • a transistor or MOSFET control input should stay off until commanded;
  • a disconnected external input should be interpreted as logic 0.

Open-drain buses are a particularly important case. I²C SDA and SCL lines, for example, are normally pulled HIGH through resistors while connected devices pull them LOW when transmitting.

The decision should also consider power-up behavior. If the correct logic state must exist before the MCU initializes, relying only on firmware configuration may not be sufficient.

In other words, choose the resistor according to what the hardware must do when software is not yet in control.
pull up vs pull down resistor

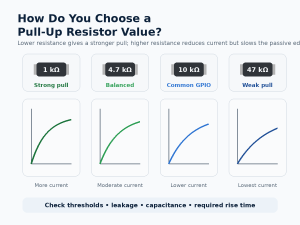
How Do You Choose a Pull Up Resistor Value?

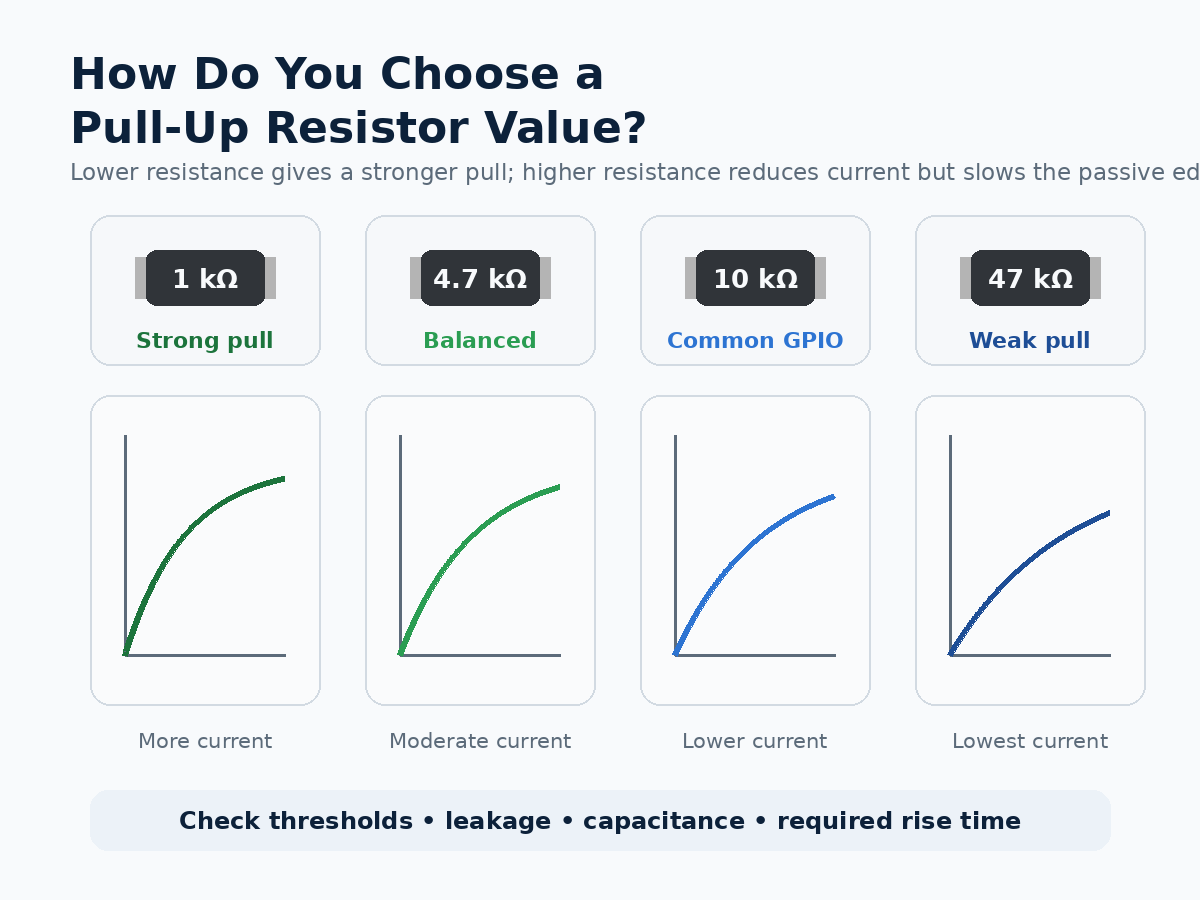
There is no universal pull up resistor value. 10 kΩ is common in slow digital-input circuits, but it should be treated as a starting point rather than a default engineering rule.

The value should be selected by checking four main factors:

  • Logic thresholds: the resulting voltage must remain inside the valid HIGH or LOW region specified by the IC.
  • Leakage current: a very high resistance can allow device leakage to shift the signal away from the intended level.
  • Current consumption: a lower resistance creates a stronger pull but increases current when another device drives the opposite state.
  • Capacitance and switching speed: resistance combines with line and input capacitance to form an RC network. Higher resistance generally produces slower passive transitions.

Typical values illustrate the tradeoff:

Resistor ValueGeneral BehaviorTypical Consideration
1 kΩStrong pull, faster edgeHigher active-state current
4.7 kΩModerate pullCommon compromise in many digital circuits
10 kΩLower currentOften suitable for low-speed GPIO
47 kΩ or higherVery low currentMore sensitive to leakage, noise, and capacitance

These are examples, not universal design values.

For I²C and other open-drain interfaces, resistor selection requires particular care because bus capacitance and rise-time limits directly affect the acceptable resistance range.

For a production PCB, the better approach is to check the IC datasheet and interface specification rather than copying a resistor value from another schematic.
pull up vs pull down resistor

Internal vs External Pull-Up and Pull-Down Resistors

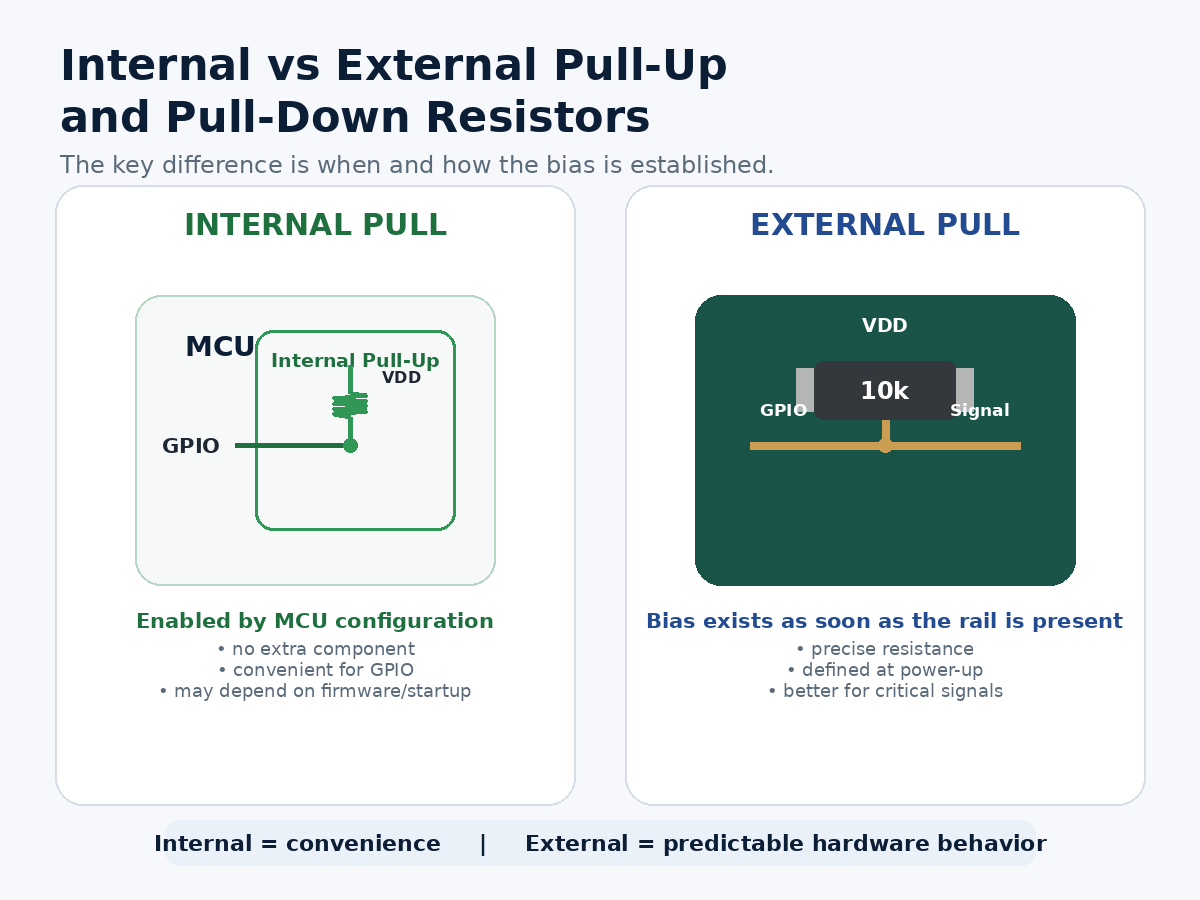
Many microcontrollers provide configurable internal pull-up and sometimes pull-down resistors. These are convenient because they reduce component count and can be enabled through the GPIO configuration.

Internal resistors are often sufficient for:

  • simple buttons and switches;
  • configuration straps;
  • low-speed GPIO inputs;
  • non-critical digital signals where the exact resistance is not important.

External resistors provide more design control.

Internal Pull ResistorExternal Pull Resistor
No additional componentRequires PCB and BOM space
Convenient for GPIOResistance can be selected precisely
Enabled by firmware/configurationCan define state immediately at power-up
Resistance may vary more widelyBetter control of current and RC timing
Good for many low-speed inputsBetter for interfaces with defined electrical requirements

The most important difference in a real product is often when the pull becomes active.

An external resistor works as soon as the relevant power rail is present. An internal resistor may not become active until the MCU reaches a particular startup state or firmware configures the GPIO.

That distinction matters for reset pins, power enables, safety-related control signals, and circuits where another IC becomes active before the main controller.

External components are also usually preferable when rise time, leakage margin, interface compliance, or resistance tolerance must be engineered rather than simply accepted.
pull up vs pull down resistor

How Are Pull-Up and Pull-Down Resistors Used in Microcontroller Circuits?

A pull up resistor in microcontroller designs can appear in many places beyond a simple pushbutton.

Common MCU applications include:

GPIO inputs.

  • A pull resistor keeps an unused or externally controlled input at a defined level until another circuit changes it.

Reset and enable pins.

  • Pull resistors establish a safe startup condition before firmware begins controlling the board.

Interrupt signals.

  • Many sensors and peripheral ICs use open-drain interrupt outputs, making a pull-up necessary to create the HIGH state.

I²C communication.

  • SDA and SCL use open-drain signaling and require pull-ups whose values suit the operating voltage, bus capacitance, and required rise time.

Configuration pins.

  • Pull-up or pull-down resistors can define boot modes, addresses, or operating states when the system powers on.

Arduino provides a familiar example. INPUT_PULLUP allows supported microcontrollers to enable an internal pull-up for a GPIO input, so a pushbutton can connect between the pin and ground. In that arrangement, the unpressed state reads HIGH and the pressed state reads LOW.

For production MCU boards, however, engineers usually need to look beyond the basic pull up resistor Arduino example. Startup timing, external peripherals, power domains, leakage, signal speed, and what happens before firmware executes can all determine whether an internal resistor is sufficient or an external component is the safer choice.

Common Pull-Up and Pull-Down Resistor Mistakes

Pull resistors are simple components, which makes them easy to overlook during schematic and PCB review. Many problems come from treating a familiar value or reference design as universally applicable.

Common mistakes include:

  • Leaving high-impedance inputs floating. An unused or externally disconnected input may need a defined bias rather than being left open.
  • Using 10 kΩ automatically. A familiar value can still be too weak, too slow, or unnecessarily strong for a particular circuit.
  • Ignoring startup behavior. An internal MCU pull may not control the signal during the earliest stage of power-up.
  • Forgetting active-low logic. With a pull-up switch input, the active condition may read LOW rather than HIGH.
  • Ignoring bus capacitance. On open-drain interfaces such as I²C, excessive resistance can produce slow rising edges.
  • Using the wrong BOM or population option. A schematic may show optional pull resistors while the production BOM or assembly drawing specifies a different DNP/populated condition.

The final check should therefore extend beyond the schematic symbol. Confirm the resistor value, voltage rail, logic polarity, startup condition, populated/DNP status, and interface requirements.

For MCU, sensor, control, and embedded PCBs, these checks are especially useful before fabrication because a small biasing error can otherwise appear later as an intermittent communication, startup, or functional-test problem.

FAQs About Pull Up vs Pull Down Resistor

Can a signal have both a pull-up and a pull-down resistor?

Yes, but the two resistors then form a voltage divider. The resulting voltage depends on their resistance ratio, so this arrangement should only be used when that intermediate bias level is intentional.

Do output pins need pull-up or pull-down resistors?

A normal push-pull output usually drives both HIGH and LOW actively, so it does not need a pull resistor for basic operation. Open-drain or open-collector outputs are different because they typically require a pull-up to create the HIGH state.

Is a 10 kΩ pull-up resistor suitable for every digital input?

No. 10 kΩ is useful in many low-speed circuits, but leakage current, logic thresholds, capacitance, switching speed, and power requirements can make another value more appropriate.

Can pull-up resistors be used with both 3.3 V and 5 V circuits?

Yes, provided the resistor connects to a voltage that is valid for every device on that signal. The pull-up voltage must not exceed the input-voltage limit of any connected IC.

Should an external pull resistor be added if the MCU already has an internal one?

Not necessarily. Internal pulls are convenient for many GPIO inputs, but an external resistor is preferable when the signal needs a defined state before firmware initialization, a specific resistance, stronger biasing, or controlled rise time.

If your MCU, sensor, industrial control, or embedded design is moving from schematic to production, you can send the Gerber/PCB files, BOM, and project requirements to sales@bestpcbs.com. EBest Circuit can support engineering review, PCB fabrication, component sourcing, PCBA assembly, testing, and quotation for the next production stage.
You may also like

COB LED Aluminum PCB Manufacturing for High-Power LED Modules

August 19th, 2026

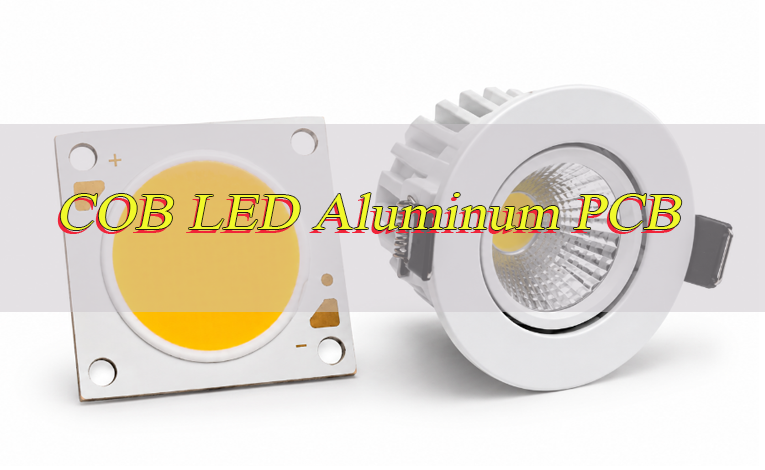
A COB LED aluminum PCB combines electrical routing with an efficient thermal path for high-power LED modules. Its performance depends on the dielectric layer, copper layout, LED interface and metal base working together. EBest Circuit supports metal core PCB projects from PCB design and prototyping to component sourcing, PCB assembly and mass production.

Are you worried about these COB LED aluminum PCB problems?

  • The COB LED still runs too hot after changing from FR4 to an aluminum PCB.
  • You are unsure which thermal conductivity, dielectric thickness or copper weight is actually needed.
  • The prototype works, but material or assembly consistency becomes difficult in production.

As a professional metal core PCB manufacturer, EBest Circuit can solve these issues by matching the PCB construction to the LED package, electrical load and thermal requirements. Below are our solutions:

  • Improve the Thermal Path
    Review the dielectric, copper spreading area and metal-base construction to reduce unnecessary thermal resistance.
  • Select the Right PCB Specifications
    Define thermal conductivity, dielectric thickness, copper weight and aluminum thickness from the actual LED power and current.
  • Keep Production Consistent
    Confirm the construction during prototyping and maintain the approved materials and assembly requirements in volume production.

Developing a high-power COB LED aluminum PCB? Send your PCB files, LED datasheet and project requirements to sales@bestpcbs.com for a quotation.

COB LED Aluminum PCB

What Is a COB LED Aluminum PCB and Why Is It Used for High-Power LEDs?

A COB LED aluminum PCB is a metal-based PCB designed to carry current and move heat away from a COB LED module. It is widely used in high-power lighting because the aluminum base can spread concentrated heat more effectively than a conventional FR4 structure.

A common single-layer construction is:

Copper circuit → thermal dielectric → aluminum base

In the finished LED module, heat typically travels through:

LED junction → LED package → solder or thermal interface → copper → dielectric → aluminum base → heat sink

The copper carries current and spreads heat around the LED area. The dielectric provides electrical isolation while transferring heat into the aluminum base, which distributes it across a larger surface.

The PCB should be designed around the actual COB LED package. Confirm the pad layout, thermal-contact area, optical center, package dimensions and mounting method from the LED datasheet before finalizing the footprint.

How Does a COB LED Aluminum PCB Improve Heat Dissipation?

A COB LED aluminum PCB spreads heat from the small COB LED area into a much larger metal surface. Heat moves through the copper and dielectric before reaching the aluminum base, so these intermediate layers directly affect thermal performance.

Three parameters matter most:

  • Dielectric Thermal Conductivity
    Higher conductivity improves heat transfer through the insulating layer. It should be evaluated together with dielectric thickness rather than used as a stand-alone specification.
  • Dielectric Thickness
    A thinner dielectric generally lowers thermal resistance, but it still needs enough dielectric strength and electrical isolation for the application.
  • Effective Heat-Transfer Area
    Adequate copper and thermal-contact area helps spread heat before it crosses the dielectric. This is especially important when a high-power COB concentrates heat into a small footprint.

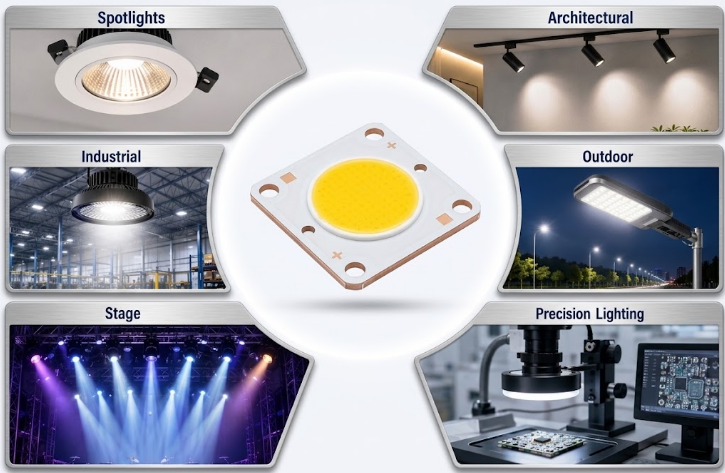
Which Applications Use COB LED Aluminum PCBs and COB Light Engines?

COB LED aluminum boards are mainly used where high light output and concentrated heat occur in the same compact assembly.

Typical applications include:

  • Spotlights and Downlights: Compact products with limited space for the PCB and cooling structure.
  • Track and Architectural Lighting: Modules requiring stable output and accurate LED positioning.
  • High-Bay and Industrial Lighting: Higher-power products designed for long operating periods.
  • Streetlights and Floodlights: Outdoor lighting exposed to high power and elevated enclosure temperatures.
  • Stage Lighting: High-output sources operating at relatively high current.
  • Machine-Vision Lighting: Applications where stable illumination affects imaging and inspection quality.
  • Optical Inspection Equipment: Systems requiring precise LED positioning relative to optics.
  • Medical Illumination: Compact lighting modules requiring stable operation and repeatable assembly.
  • Projector and Imaging Light Sources: High-brightness systems with concentrated thermal loads.
  • COB Light Engines: Integrated modules combining the LED, PCB, optics and cooling structure.

For a COB LED module aluminum PCB, total LED power, operating time, ambient temperature and available cooling area matter more than the number of LEDs alone.

COB LED Aluminum PCB Application

How Should Thermal Conductivity, Dielectric Thickness and Copper Weight Be Selected?

For a COB LED aluminum PCB, these values should follow the LED power, operating current, thermal target and electrical-isolation requirement.

  • Select Thermal Conductivity From Heat Density
    Higher thermal conductivity is useful when the COB LED produces concentrated heat or when PCB area is limited. Moderate-power designs may not require the highest thermal class.
  • Keep the Dielectric Thin Without Sacrificing Isolation
    A thinner dielectric lowers thermal resistance, but it still needs to meet operating-voltage, dielectric-strength and manufacturing requirements.
  • Match Copper Weight to Current and Geometry
    Higher current may require heavier copper, but trace width and available copper area are equally important. Heavy copper does not correct an undersized current path.
  • Provide Enough Copper Around the Heat Source
    Larger copper areas around the COB LED improve lateral heat spreading before heat passes through the dielectric.
  • Avoid Increasing Specifications Without Finding the Limitation
    A higher W/m·K material or heavier copper provides little benefit if another part of the PCB construction limits thermal performance.
  • Validate the Construction During Prototyping
    Test the selected copper and dielectric construction at the intended LED power before freezing the design for production.

How Should the COB LED Footprint and Thermal Pad Match the Aluminum PCB?

Use the actual COB LED package drawing rather than a generic footprint. Similar-sized COB LEDs can have different electrical pads, thermal regions and mounting structures.

Check the following before release:

  • Electrical Pads: Match pad dimensions, spacing and polarity to the datasheet.
  • Thermal-Contact Area: Align the PCB thermal region with the package structure.
  • Optical Center: Position the emitting area correctly relative to the lens or reflector.
  • Solder Mask Clearance: Keep solderable areas fully exposed.
  • Package Outline: Leave enough clearance around the LED body.
  • Mounting Holes: Align the PCB with the LED module and heat sink.
  • Keep-Out Areas: Keep components and hardware away from optical or mounting areas.
  • Heat-Sink Interface: Maintain a flat and consistent backside contact area where required.

For soldered packages, solder volume also matters. Too much solder can increase stand-off or tilt the LED, while large voids under the thermal region reduce effective heat transfer.

Stencil openings, paste volume and reflow conditions should therefore be matched to the thermal-pad geometry.

When Should You Choose an Aluminum-Core PCB Instead of a Copper-Core PCB for COB LEDs?

Use an aluminum-core PCB when the required LED temperature can be achieved with the correct dielectric and cooling structure. Move to copper only when the thermal demand exceeds what an optimized aluminum MCPCB can support.

Choose an aluminum-core PCB when:

  • The Heat Density Is Within the Range of a Conventional MCPCB
    Aluminum works well for many spotlights, downlights, industrial lights, streetlights and other high-power LED modules.
  • The Dielectric Can Meet the Thermal Target
    If the correct dielectric conductivity and thickness provide enough thermal performance, a copper base adds limited value.
  • PCB Weight Matters
    Aluminum is lighter than copper and is suitable for larger lighting assemblies.
  • A Standard MCPCB Structure Is Preferred
    Aluminum-core PCB is widely used for both prototypes and volume LED production.
  • The External Cooling System Is Adequate
    If heat can move effectively from the PCB into the final cooling structure, aluminum is usually sufficient.

Consider a copper-core PCB when:

  • The COB LED Produces Very High Local Heat Flux
    A highly concentrated thermal load may benefit from stronger lateral heat spreading.
  • An Optimized Aluminum PCB Still Runs Too Hot
    Copper becomes more relevant after the dielectric and other major thermal limitations have already been addressed.
  • The Design Requires a Very Low-Resistance or Direct Thermal Path
    Some specialized LED constructions use copper-based structures to shorten the path between the heat source and metal substrate.
  • Thermal Performance Matters More Than Weight
    Copper provides higher bulk thermal conductivity but also increases PCB weight.

Use aluminum when it meets the thermal target. Move to copper only when the optimized aluminum structure is no longer sufficient.

What Steps Are Used to Manufacture and Assemble a High-Power COB LED Aluminum PCB?

A high-power COB LED aluminum PCB needs a controlled manufacturing process so the approved material, circuit and mechanical structure remain consistent through assembly.

Step 1: Review the Design and Material Requirements

Confirm the COB LED footprint, copper weight, dielectric, aluminum thickness, board dimensions, mounting holes, surface finish and required thermal interface.

Step 2: Prepare the Aluminum-Based Laminate

Use the approved copper, dielectric and aluminum construction. Material substitutions should be reviewed before production because they can change thermal and mechanical performance.

Step 3: Form and Etch the Copper Circuit

Image and etch the LED pads, power paths and supporting circuitry. Trace width and spacing must be compatible with the selected copper thickness.

Step 4: Drill and Profile the PCB

Produce mounting holes, slots and the finished outline according to the mechanical drawing. These features may align directly with the heat sink, lens holder or enclosure.

Step 5: Apply Solder Mask and Surface Finish

Keep COB LED pads and other solderable areas correctly exposed. The surface finish should match the intended assembly process.

Step 6: Print Solder Paste and Place Components

Control paste volume around the LED pads and place the COB LED accurately. Positioning may affect both electrical connection and optical alignment.

Step 7: Complete Reflow and Assembly Inspection

Use an appropriate reflow profile and check solder wetting, component orientation, stand-off and visible defects after soldering.

Step 8: Mount the PCB to the Cooling Structure

Install the assembled PCB using the specified TIM, screws or clamping arrangement. Avoid uneven contact or mechanical stress on the LED package.

Step 9: Verify Electrical and Thermal Performance

Operate the assembled module at the specified load and confirm current, LED function and operating temperature before volume production.

COB LED Aluminum PCB Manufacturing

What Steps Are Used to Inspect and Test a COB LED Aluminum PCB Before Shipment?

Inspection should cover the characteristics that can affect electrical operation, assembly fit and heat transfer.

Step 1: Verify Material and PCB Construction

Check the aluminum base, dielectric, copper thickness and finished PCB thickness against the approved specification.

Step 2: Check Dimensions and Mounting Features

Inspect the PCB outline, slots, mounting holes and critical dimensions to confirm fit with the mechanical assembly.

Step 3: Inspect Circuit and Surface Quality

Use visual inspection and AOI where applicable to identify opens, shorts, damaged pads, contamination, scratches or solder-mask registration defects.

Step 4: Perform Electrical and Insulation Testing

Verify circuit continuity and electrical isolation between the copper circuit and aluminum base.

Step 5: Check PCB Flatness

Inspect flatness when the PCB backside forms part of the thermal interface. Excessive warpage can reduce contact with the cooling surface.

Step 6: Inspect COB LED Placement and Soldering

Verify polarity, orientation, LED position, solder wetting and the condition of the main thermal-contact area.

Step 7: Perform Functional Testing

Operate the assembled module under the specified electrical conditions. Check for abnormal brightness, flicker, current behavior or other functional problems.

Step 8: Complete Thermal Validation

Test the module with the intended or representative cooling structure until temperature approaches a stable condition. Use thermocouples, thermal imaging or the LED manufacturer’s recommended method where appropriate.

Step 9: Confirm Production Consistency

Check that production boards use the approved materials, PCB construction and assembly requirements established during prototype validation.

COB LED Aluminum PCB Testing

What COB LED Aluminum PCB Manufacturing Capabilities Can We Provide?

Manufacturing capability determines whether the required COB LED aluminum PCB construction can be produced consistently from prototype to volume production. The table below summarizes our main MCPCB process capabilities for design and manufacturing reference.

ItemCapabilities
Maximum Layer CountUp to 10 layers
PCB Thickness0.3–4.0 mm
Maximum Board SizeUp to 610 × 1220 mm (24 × 48 in.)
Copper Weight0.5–10 oz
Minimum Trace / Space0.15 / 0.15 mm (6 / 6 mil)
Minimum Hole Diameter0.30 mm (12 mil)
Minimum Punch Hole Diameter3.0 mm (0.12 in.)
Minimum Hole Spacing0.40 mm (16 mil)
Maximum Aspect Ratio12:1
Minimum Solder Pad Diameter0.40 mm (16 mil)
Thermal Conductivity0.8–1.5 W/m·K standard; 2.0–6.0 W/m·K high thermal conductivity
Warp and Twist< 0.75%
FlammabilityUL 94V-0
Thermal Stress6 × 10 sec at 288°C
Surface FinishENIG, Flash Gold, Hard Gold, Selective Gold Plating, HASL, Lead-Free HASL, OSP, Immersion Silver, Immersion Tin

Case Study: High-Power COB LED Aluminum PCB From Prototype to Production

Project Background

A high-power COB LED module required an aluminum PCB connected to an external heat sink. The board had to provide a reliable thermal path while maintaining the correct LED position, mounting-hole alignment and mechanical fit.

Project Requirements

The PCB needed to:

  • Carry the required COB LED current
  • Transfer heat effectively to the cooling structure
  • Use an appropriate dielectric, copper weight and aluminum base
  • Match the LED footprint and thermal-contact area
  • Maintain PCB flatness and mounting accuracy
  • Support prototype assembly and later production

Our Solution

EBest Circuit reviewed the COB LED datasheet, PCB layout and mechanical drawing before prototype fabrication.

The main actions included:

  • Matching the COB LED footprint and thermal area to the package
  • Reviewing dielectric thickness, copper weight and aluminum construction
  • Providing sufficient copper around the main heat source
  • Controlling PCB flatness and mounting-hole alignment
  • Checking soldering, TIM contact and mechanical fit during prototype assembly
  • Maintaining the approved construction for production

Results

Prototype validation confirmed:

  • Stable COB LED mounting and alignment
  • Consistent PCB-to-heat-sink contact
  • A controlled thermal path
  • Reliable electrical and assembly performance
  • A repeatable construction for volume production

The approved PCB construction and assembly requirements were then carried forward into production.

What Specifications and Files Are Required for a COB LED Aluminum PCB Quote?

For a COB LED aluminum PCB quote, provide:

Bare PCB:

  • Gerber files
  • NC drill files
  • Board dimensions
  • Mechanical drawing
  • Finished PCB thickness
  • Copper weight
  • Aluminum thickness
  • Thermal conductivity requirement
  • Dielectric thickness or material requirement
  • Surface finish
  • Solder mask requirement
  • Quantity
  • Special tolerance or testing requirements

PCB Assembly:

  • BOM
  • Pick-and-place file
  • Assembly drawing
  • COB LED part number and datasheet
  • Polarity information
  • Functional-test requirements

For Thermal Review:

  • LED operating power and current
  • Heat-sink drawing
  • TIM specification
  • Mounting method
  • Expected ambient temperature
  • Maximum allowable operating temperature

If some specifications are still open, send the available project files first for review.

Why Choose EBest Circuit for COB LED Aluminum PCB Manufacturing?

With more than 20 years of PCB manufacturing experience, EBest Circuit supports COB LED aluminum PCB projects from prototypes through mass production.

  • One Supplier From Prototype to Production
    PCB prototyping, Metal Core PCB manufacturing, component sourcing and PCB assembly can be coordinated through EBest Circuit, reducing supplier handoffs.
  • Metal Core PCB Manufacturing
    Our PCB range includes Metal Core PCB / MCPCB, supporting COB LED modules and other thermal-management applications.
  • Capacity for Volume Production
    EBest Circuit has approximately 260,000 sq. ft. (28,900 m²) of monthly PCB manufacturing capability.
  • Support for Urgent Projects
    Expedited service is available for eligible projects, with qualifying urgent boards capable of shipment within 24 hours after requirements are confirmed.
  • Quality and Compliance
    EBest Circuit holds ISO 9001:2015, IATF 16949, ISO 13485:2016, AS9100D, UL, RoHS and REACH credentials.

Welcome to contact us if you have any request for COB LED aluminum PCB.

FAQs About COB LED Aluminum PCBs

Q1: Does a COB LED need a constant-current driver?
A1: Usually yes. A high-power COB LED is normally driven by a constant-current driver so current remains controlled as forward voltage changes. If the module already includes current regulation, follow its datasheet.

Q2: Should multiple COB LEDs be connected in series or parallel?
A2: Series connection is generally easier to control because each COB receives the same current. Parallel branches need current balancing because forward-voltage differences can produce unequal current sharing.

Q3: How should the LED driver voltage range match a COB LED?
A3: The driver’s output-voltage range must cover the forward voltage of the COB LED or complete LED string. Add the forward voltages of series-connected COB LEDs before selecting the driver.

Q4: Can a high-power COB LED be dimmed with PWM?
A4: Yes, when the driver supports it. Use the dimming method specified by the driver manufacturer rather than switching LED power directly.

Q5: Is it better to run a COB LED below its maximum rated current?
A5: Often yes. Lower current reduces thermal load and provides more operating margin. Select the working current from the LED manufacturer’s current, temperature and light-output data.

Q6: Can a COB LED be connected or disconnected while the driver is powered?
A6: It is better to avoid it. Hot-plugging can expose the COB LED to electrical transients. Turn the driver off unless the system is specifically designed for hot swapping.

Q7: Can a reflector or lens touch the COB LED?
A7: Optical parts should not press directly against the emitting surface or electrical contacts. Use a suitable holder to maintain alignment and prevent damage.

Q8: Can a failed COB LED be replaced on the MCPCB?
A8: In many designs, yes. Replaceability depends on the attachment method and thermal mass of the MCPCB. Rework temperature and heating time need careful control.

Q9: Should a high-power COB LED system include overtemperature protection?
A9: It is useful when cooling conditions can vary. Temperature sensing can reduce LED current or shut the system down if temperature exceeds the defined limit.

Q10: What happens if one parallel COB LED branch fails open?
A10: The remaining branches may carry more current when they share one constant-current source. Parallel designs should consider current balancing or independent current regulation.

Conclusion

A reliable COB LED aluminum PCB depends on the dielectric, copper layout, LED interface and metal substrate being matched to the actual electrical and thermal load.

EBest Circuit supports metal core PCB manufacturing, prototyping, component sourcing, PCB assembly and mass production. For a high-power COB LED aluminum PCB, COB LED module or light engine project, send your files and requirements to sales@bestpcbs.com for a quotation.

You may also like

Power Resistor: How It Works and How to Choose One

August 19th, 2026

A power resistor is used when a circuit needs to dissipate more electrical energy than a standard signal-level resistor can comfortably handle. These components are common in power supplies, motor drives, battery systems, inverters, charging equipment, and industrial controls, where current, voltage, or transient energy can generate substantial heat.

Choosing the right power resistor involves more than matching the resistance value. Power rating, working voltage, pulse capability, operating temperature, construction, and mounting conditions all affect performance. This guide explains how power resistors work and what to consider when selecting one for a real circuit.

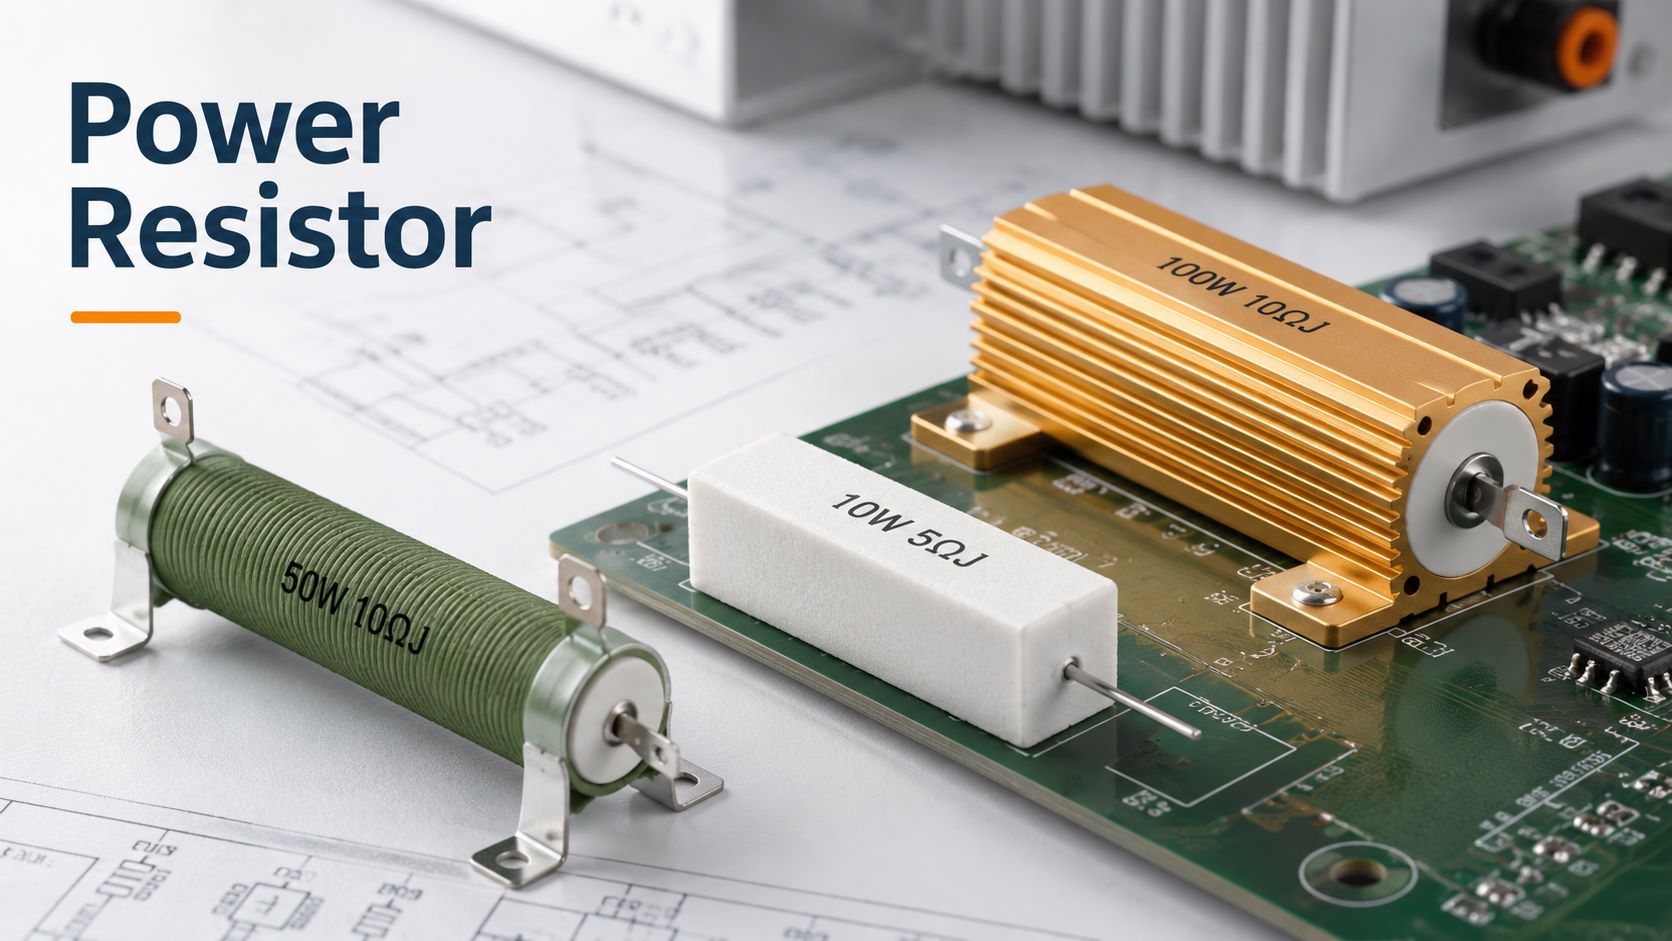
power resistor

What Is a Power Resistor?

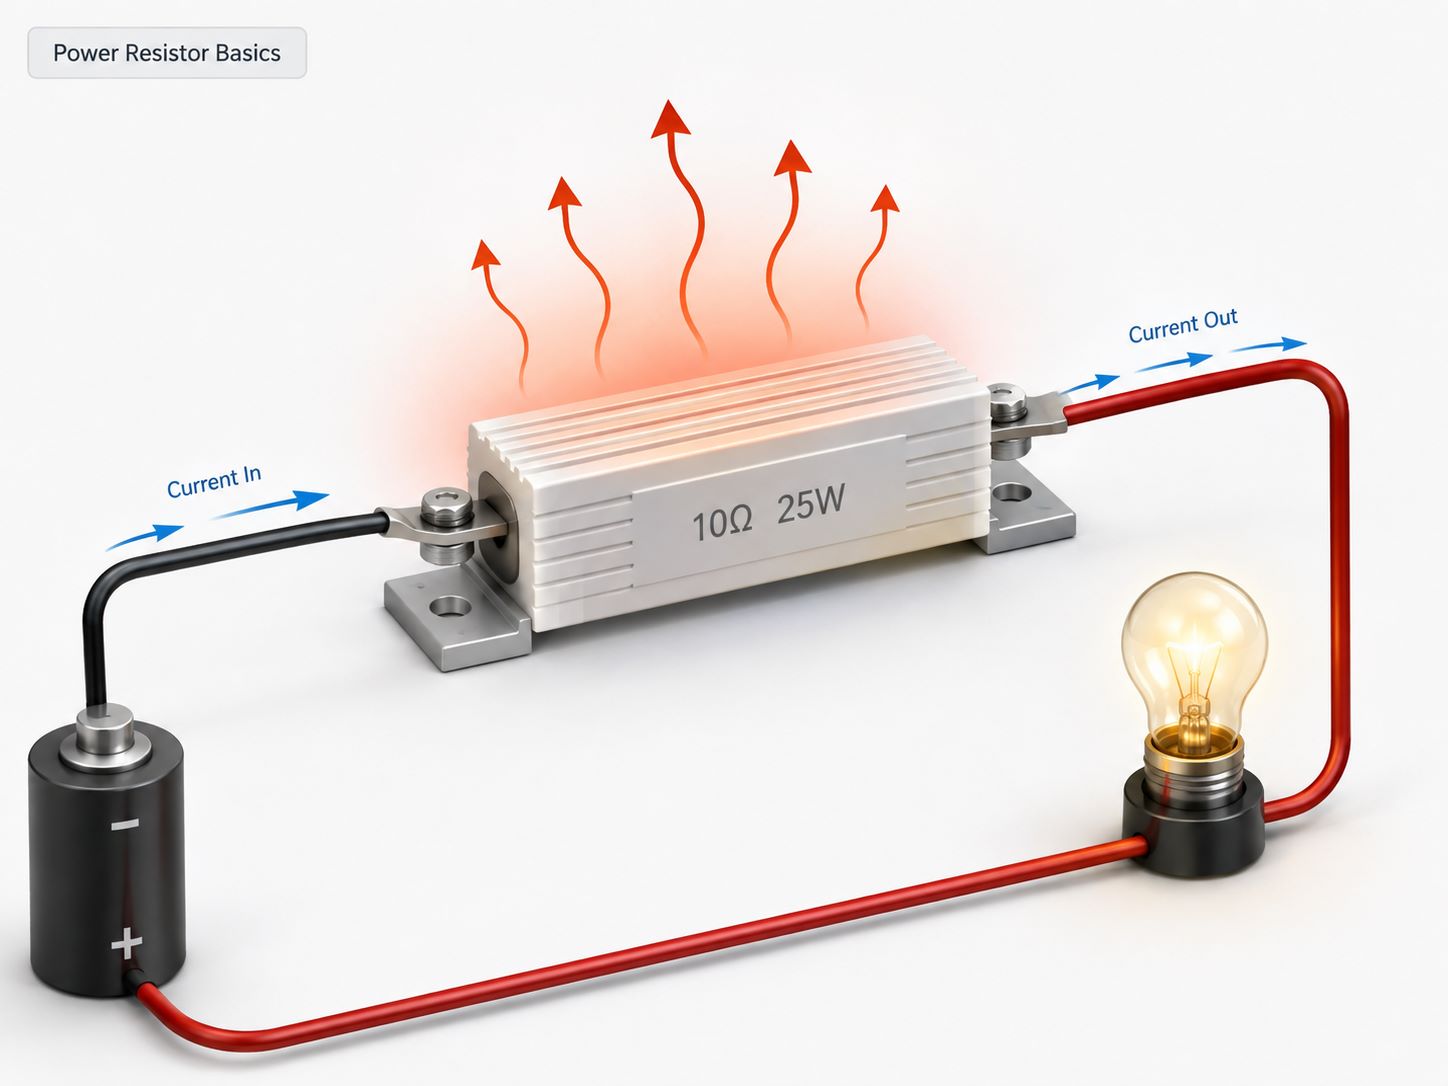
A power resistor is a resistor designed to dissipate relatively large amounts of electrical power as heat while maintaining its specified resistance.

Like other resistors, it limits current or creates a controlled voltage drop. The main difference is its ability to manage a higher thermal load.

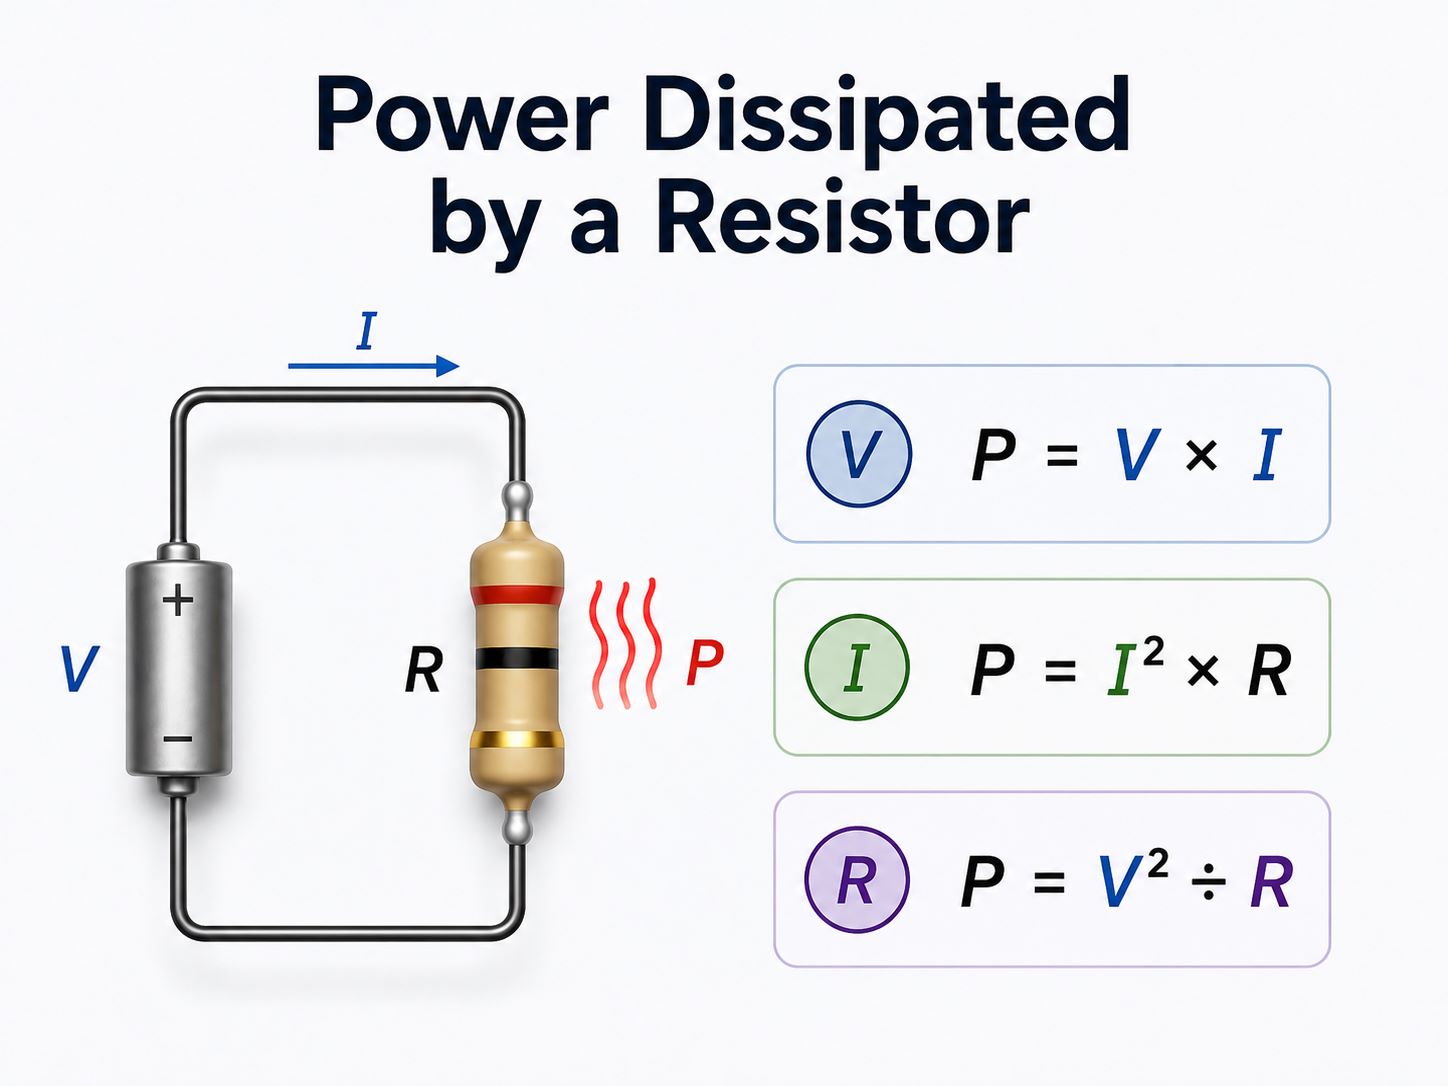
The basic power relationships are:

  • P = V × I
  • P = I² × R
  • P = V² ÷ R

Where P is power, V is voltage, I is current, and R is resistance.

For example, if 2 A flows through a 10 Ω resistor:

P = 2² × 10 = 40 W

The resistor must therefore manage about 40 W of heat under that operating condition.

This does not mean a 40 W resistor should automatically be selected. Continuous operation near the maximum rating may leave little thermal margin, especially inside a warm enclosure or without sufficient airflow.

Power resistors use different constructions to move heat away from the resistive element. Depending on the component, heat may be released into the surrounding air, transferred through the PCB, or conducted into a chassis or heatsink.

power resistor

When to Use a High Power Resistor?

A high power resistor is appropriate when continuous power, pulse energy, or operating temperature exceeds what a conventional resistor can safely handle.

There is no universal wattage at which a resistor becomes “high power.” The required rating depends on the application.

Typical situations include:

  • capacitor discharge;
  • inrush current limiting;
  • motor braking;
  • load testing;
  • current limiting;
  • repeated pulse absorption;
  • high-temperature operation.

A higher wattage rating does not cause a resistor to consume more power. Circuit conditions determine the actual dissipation.

For example, a 100 Ω resistor with 10 V across it dissipates:

P = 10² ÷ 100 = 1 W

A 2 W, 5 W, or 20 W version would still dissipate approximately 1 W in the same circuit. The higher-rated resistor simply provides more thermal capacity.

When choosing a high wattage resistor, however, wattage should not be the only consideration. Maximum working voltage, pulse rating, inductance, physical size, and mounting method can be equally important.

For switching circuits or repetitive pulses, check the manufacturer’s overload or pulse-energy data rather than relying only on the continuous power rating.

Which Type of Resistor Is Used for High Power Applications?

The best resistor for a high-power application depends on continuous wattage, pulse energy, available space, required precision, and thermal conditions.

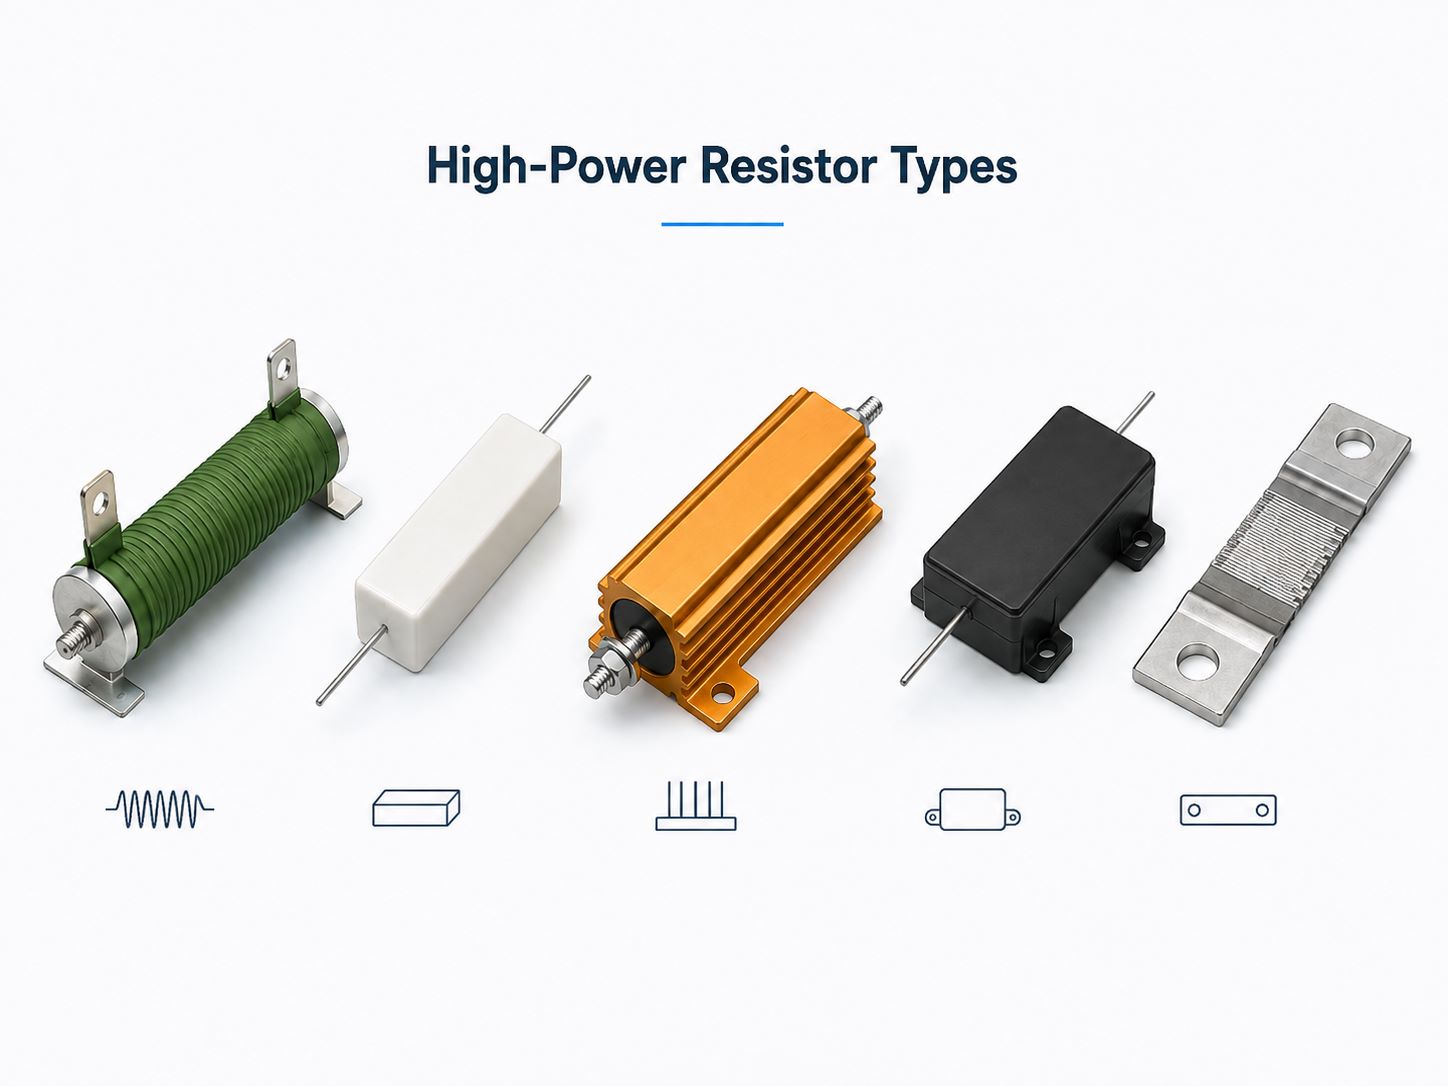
Wirewound resistors

  • Wirewound resistors offer good power handling and overload capability. They are widely used in motor drives, power supplies, braking systems, and load banks. Their wound construction can introduce inductance, so low-inductance designs may be preferred in fast-switching circuits.

Ceramic or cement resistors

  • A ceramic resistor or cement resistor provides a robust and economical option for current limiting, discharge circuits, snubbers, and general power electronics.

Aluminum-housed resistors

  • These resistors transfer heat efficiently into a chassis or heatsink. They are useful when relatively high continuous power must be handled in a compact space.

Thick-film power resistors

  • Thick-film designs can combine compact size, relatively high resistance values, and low inductance, making them useful in modern power electronics.

Foil resistors

  • A foil resistor is more suitable when power handling must be combined with tight tolerance or low temperature coefficient.

There is therefore no single answer to which type of resistor is used for high power applications. The correct choice depends on whether the main design constraint is heat, pulse energy, precision, size, or high-frequency behavior.

power resistor

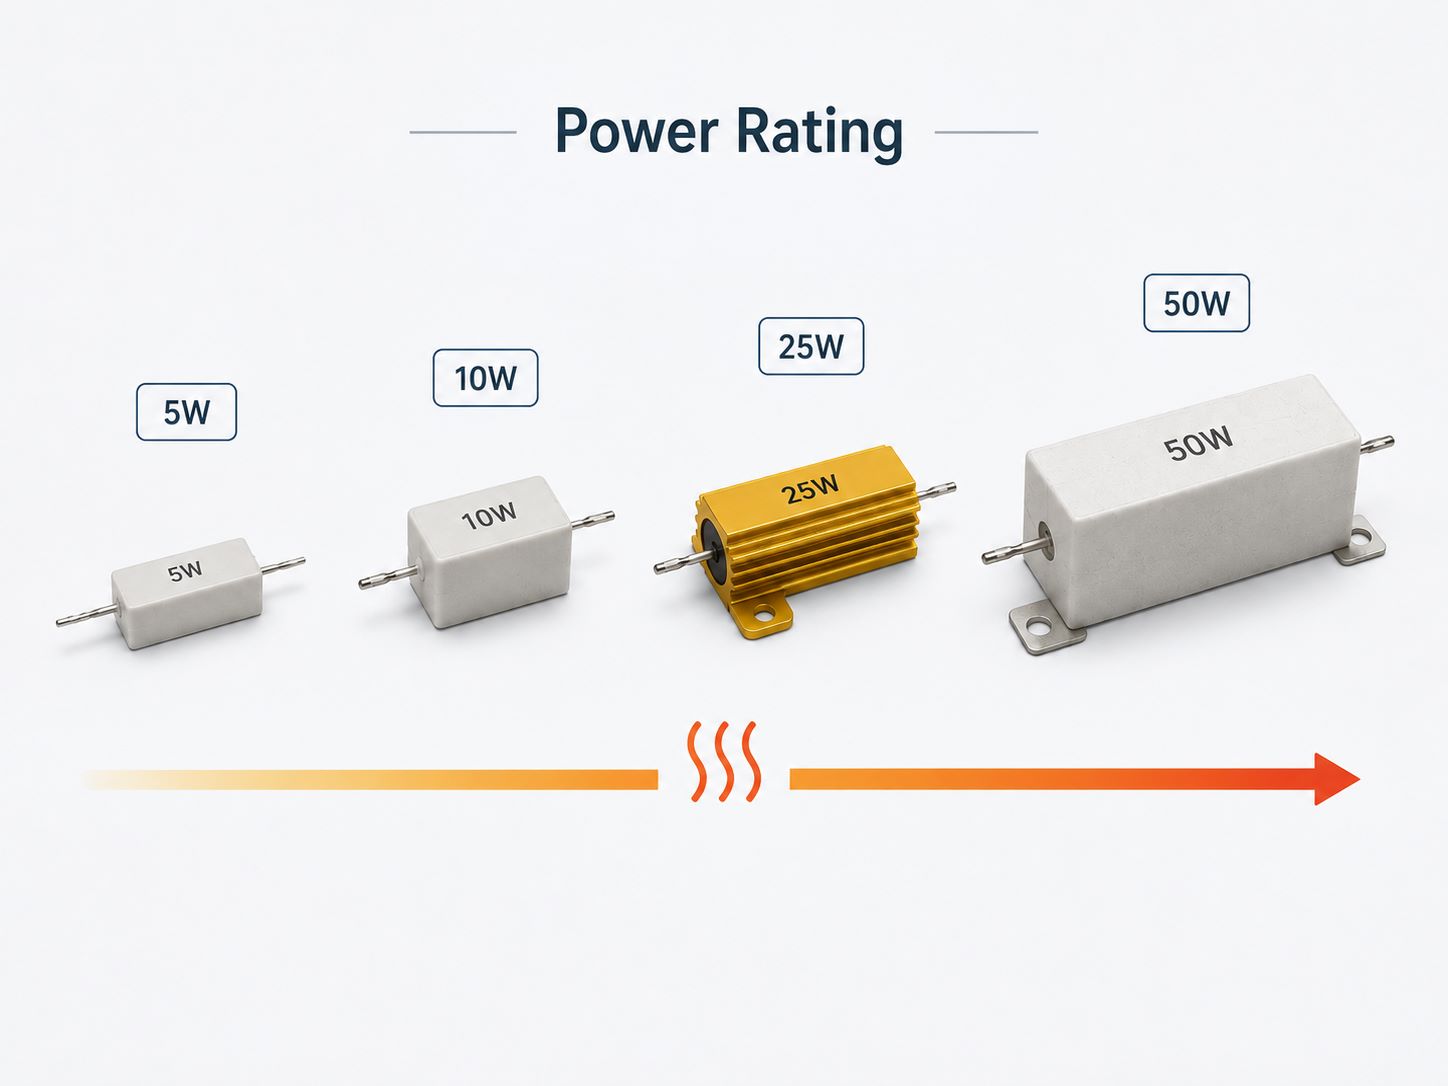
What Is a Resistor Power Rating?

A resistor power rating indicates how much electrical power a resistor can dissipate under specified conditions without exceeding its allowable temperature.

Power ratings are normally expressed in watts. Common values range from fractions of a watt to tens, hundreds, or even thousands of watts for industrial resistor assemblies.

A 50 W resistor rated power, however, does not necessarily mean the component can continuously dissipate 50 W under every condition.

The published rating may assume:

  • a defined ambient or case temperature;
  • sufficient airflow;
  • a particular PCB layout;
  • mounting on a metal chassis;
  • installation on a specified heatsink.

As temperature increases, allowable power usually decreases. This relationship is shown in the manufacturer’s derating curve.

A practical selection should therefore satisfy:

Actual power dissipation < Allowable power under real operating conditions

The nominal wattage is only the starting point.

Continuous-load designs should also leave suitable thermal margin, while pulse applications require separate verification of pulse duration, repetition rate, and overload capability. A resistor that can dissipate 50 W continuously is not automatically suitable for every short high-energy pulse.

power resistor

How to Calculate Power Dissipated by a Resistor?

The power dissipated by a resistor can be calculated from voltage, current, and resistance.

Use the equation that matches the values already known:

  • P = V × I
  • P = I² × R
  • P = V² ÷ R

For example, if a 20 Ω resistor carries 1.5 A:

P = 1.5² × 20 = 45 W

This means the resistor dissipates about 45 W.

This power resistor formula works well for steady DC conditions. Pulsed loads require an additional check because average power does not fully describe short-duration thermal stress.

For pulse applications, consider:

  • peak power;
  • pulse width;
  • repetition frequency;
  • duty cycle;
  • pulse energy.

A resistor may experience very high instantaneous power for a few milliseconds while still showing a much lower average wattage.
For this reason, repetitive pulse applications should be checked against the manufacturer’s pulse-power or pulse-energy curves. This is particularly important in precharge circuits, capacitor discharge systems, motor drives, and switching power supplies.

For steady loads, calculate the actual resistor power first. For pulsed loads, calculate the power and then verify whether the resistor construction can survive the pulse profile.

power resistor

Do Resistors Have Voltage Ratings?

Yes. Resistors do have voltage ratings, and the voltage limit can become important even when power dissipation remains within the resistor’s wattage rating.

Power and voltage ratings describe different design limits.

For example, a high-resistance component may carry very little current, so its calculated power remains low. At the same time, a high voltage across the resistor may exceed its maximum working-voltage specification.

The voltage associated with resistance and power can be estimated using:

V = √(P × R)

However, the result still needs to be compared with the manufacturer’s specified maximum working voltage.
In practice, the lower limit governs:

  • voltage allowed by the power rating; or
  • specified maximum working voltage.
High-voltage designs should also consider PCB creepage and clearance, terminal spacing, resistor body construction, contamination, and transient voltage.
When a single resistor cannot withstand the required voltage, several resistors may be connected in series to distribute the voltage stress, provided their power and voltage ratings are both checked.
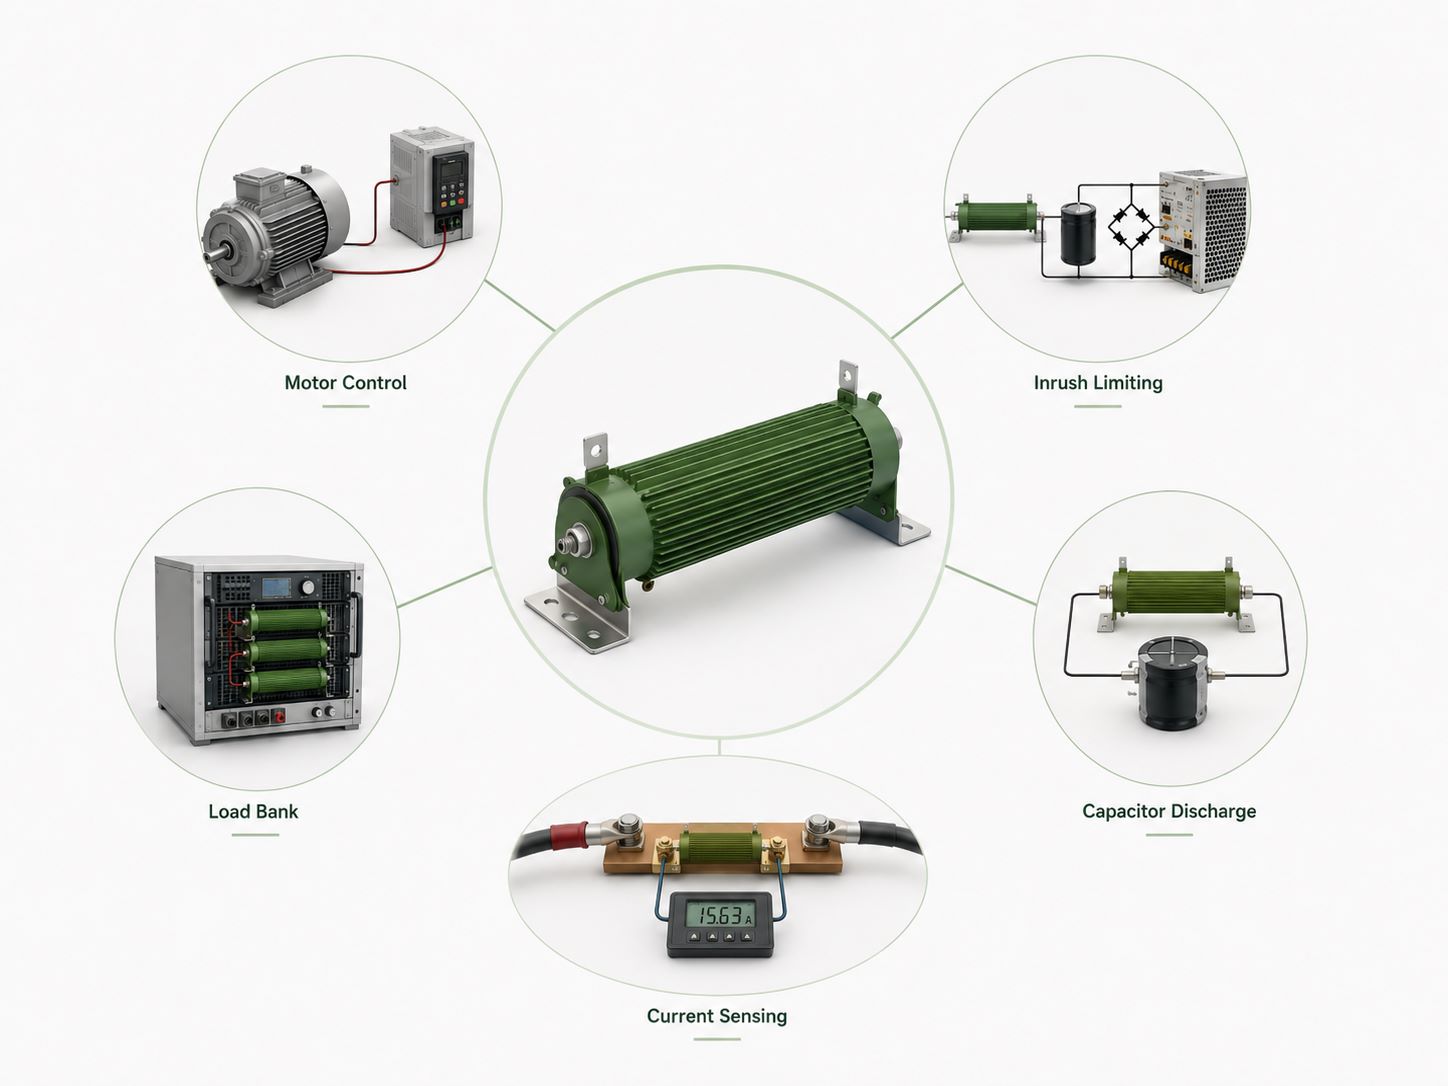
What Are Power Resistors Used For?

Power resistors are used when electrical energy needs to be limited, discharged, measured, controlled, or converted into heat.

Common power resistor applications include:

Motor braking

  • Braking resistors dissipate regenerated energy when a motor decelerates, helping control the DC bus voltage.

Inrush current limiting

  • A resistor can temporarily limit the high current drawn when large capacitors are first charged.

Capacitor discharge

  • Bleeder and discharge resistors remove stored energy from capacitors after power is disconnected.

Power supplies

  • Power resistors can provide minimum loading, voltage balancing, current limiting, and controlled energy dissipation.

Snubber and damping circuits

  • Resistors may work with capacitors to suppress ringing or absorb switching transients.

Load banks

  • Industrial resistors are commonly used to create controlled loads for testing batteries, generators, chargers, converters, and power supplies.

Current sensing

  • Low-resistance power resistors can act as shunts, producing a small voltage proportional to current.

The required resistor construction changes with the application. A braking resistor prioritizes energy and heat handling, while a current-sense resistor may prioritize low resistance, accuracy, and temperature stability.

power resistor

Can I Use a Higher Wattage Resistor?

Yes, in many circuits a higher-wattage resistor can replace a lower-wattage resistor when the other specifications remain suitable.

For example, a 100 Ω, 5 W resistor can often replace a 100 Ω, 2 W resistor. If the circuit produces 1 W of dissipation, the 5 W component still dissipates approximately 1 W. Its higher rating simply provides additional thermal margin.

Before using a higher wattage resistor, check:

  • resistance value;
  • tolerance;
  • maximum working voltage;
  • pulse rating;
  • temperature coefficient;
  • inductance;
  • physical size;
  • mounting requirements.

This matters because two resistors with the same resistance but different wattage ratings may use different constructions.

A larger wirewound resistor, for example, may introduce more inductance than a smaller low-inductance component. A chassis-mounted resistor may also achieve its published power rating only when installed on an appropriate metal surface.

So, can I use a higher wattage resistor? Usually yes—but wattage should not be considered in isolation.

Choose enough power margin for the real operating environment without unnecessarily increasing size, cost, or parasitic effects.

FAQs About Power Resistor

Is it normal for a power resistor to get very hot?

Yes. Power resistors convert electrical energy into heat, so high surface temperature can be normal. Check the datasheet temperature limit and derating curve rather than judging by touch alone.

How much wattage margin should I leave when choosing a power resistor?

There is no fixed margin for every design. Calculate the actual dissipation first, then select a resistor with enough headroom based on ambient temperature, cooling, duty cycle, and the manufacturer’s derating data.

Can I use several lower-wattage resistors instead of one high-power resistor?

Yes. Series, parallel, or series-parallel networks can share the load, provided the total resistance is correct and each resistor stays within its own power and voltage limits.

Can a power resistor briefly exceed its continuous wattage rating?

Sometimes. Short pulses may exceed the continuous rating if the resistor’s pulse or overload specification allows it. Always check pulse width, energy, repetition rate, and the manufacturer’s pulse curve.

Does a power resistor need a heatsink?

Not always. Some power resistors work in free air, while aluminum-housed or chassis-mounted types may need a heatsink or metal surface to achieve their rated power.

Planning a Power Resistor PCB or PCBA Project? If your project involves power resistors, high-current circuits, thermal design, or PCBA assembly, our engineering team can review your PCB files, BOM, and key requirements before production. You are also welcome to visit our factory to see our PCB and PCBA manufacturing process, production lines, and quality control in person. Send your project details or arrange a factory visit at sales@bestpcbs.com.

You may also like

Shunt Resistor Selection and PCB Layout for Accurate Sensing

August 18th, 2026

A shunt resistor circuit can be correct on the schematic and still produce inconsistent readings on assembled boards. At milliohm resistance levels, the PCB copper, pad entry, solder joints, temperature, and measurement nodes can contribute error that the basic calculation never shows.

The safest approach is to treat the shunt resistor, PCB layout, BOM, and acceptance test as one measurement system. This guide shows what to calculate, what to inspect in the layout, what to lock before purchasing, and what evidence to request from the PCBA build.

shunt resistor

What Is a Shunt Resistor?

A shunt resistor, also called a current sense resistor, is a low-value resistor placed in the load-current path. Using a shunt resistor for measuring current is straightforward in principle: current creates a proportional voltage across the part. The voltage across it is proportional to current: V = I × R. A current-sense amplifier or ADC reads that voltage and converts it into a measurement or protection decision.

At 1 mΩ, every ampere produces only 1 mV. That makes the physical sense points important: copper, pads, solder joints, and amplifier offset can become a meaningful share of the signal. A precise component does not guarantee a precise assembled measurement.

Define three groups of requirements before selecting the part:

  • Electrical range — minimum, normal, maximum, surge, and fault current.
  • System limits — permitted voltage drop, power loss, response time, and accuracy over temperature.
  • Architecture — high-side or low-side sensing and a two-terminal or four-terminal shunt.

How Does Shunt Resistor Current Measurement Work?

A 2 mΩ shunt carrying 30 A gives three immediate results:

  • 60 mV across the shunt — confirm that the load can tolerate this voltage loss.
  • 1.8 W in the resistor — verify the derated thermal capacity in the real enclosure.
  • 2.4 V after a gain of 40 — confirm amplifier and ADC headroom, including faults and tolerances.

Accuracy must then be checked as a chain. Resistor tolerance sets the starting error. Temperature coefficient changes the resistance as the part heats. Amplifier offset becomes significant when the sense voltage is small. Gain error, ADC reference error, noise, and any copper included between the real sense points add further uncertainty.

Do not specify accuracy only at room temperature and nominal current. Define at least a low-current point, a normal operating point, and a high-current point after thermal stabilization. If the circuit also protects against faults, add the trip current, response time, and allowed recovery behavior. These become the basis of calibration and production testing.

Use the symptom to narrow the cause. A large percentage error at low current usually points first to offset, noise, or incorrect sense points. Drift that appears only after high-current warm-up points more strongly to shunt TCR, temperature rise, or heated copper. A consistent gain error across the range may be calibratable; unstable board-to-board variation usually requires a material, layout, assembly, or fixture investigation.

shunt resistor

How Do You Select a Shunt Resistor?

Calculate a provisional resistance from the maximum sense voltage divided by maximum current. A shunt resistor calculator can speed up the resistance and power calculation, but it cannot validate thermal margin, pulse capability, PCB copper, or sense-point placement. Then calculate continuous power with P = I²R and pulse energy for overload events. Apply the component manufacturer’s derating curve rather than assuming the printed wattage is available under every PCB and airflow condition.

Next compare tolerance, TCR, pulse rating, terminal design, package, land pattern, operating temperature, and supply status. For example, a low TCR helps control drift, but it does not compensate for a hot copper neck-down beside the resistor or a sense trace connected outside the intended terminal point.

Lock these purchasing decisions in the RFQ and BOM:

  • State the exact manufacturer part number and whether substitutions are prohibited or require approval.
  • For any alternate, require matching resistance, tolerance, TCR, continuous and pulse ratings, terminal structure, package, and recommended footprint.
  • Name the person who must approve an alternate before components are purchased or loaded onto the SMT line.

This prevents a common failure: accepting a resistor because its nominal value and package appear correct, while its thermal behavior, pulse capability, or terminal geometry changes the actual measurement and assembly result.

Shunt Resistor vs Hall Effect Sensor

Choose a shunt when the product can tolerate a small voltage drop and needs a compact, fast, cost-effective measurement. Consider a Hall effect sensor when galvanic isolation or lower conductive loss is more important. Neither option is automatically more accurate; each moves the dominant errors to different parts of the system.

DecisionShunt resistorHall effect sensor
IsolationNo inherent galvanic isolationIsolated options available
Power lossI²R loss in the load pathLow conductive insertion loss
Key error sourcesTCR, offset, copper, sense-point locationOffset, magnetic noise, external fields
PCB prioritiesCurrent path, Kelvin routing, heatFootprint, supply, magnetic clearance
Best fitDirect, compact measurement where loss is acceptableIsolation or low conductive loss is required

For procurement, compare the complete implementation rather than component price alone. A shunt solution needs controlled copper, Kelvin sensing, heat management, and a suitable amplifier. A Hall solution may need more board area, supply routing, magnetic clearance, and calibration. The approved architecture should reflect isolation, bandwidth, accuracy, fault response, space, and lifecycle requirements.

Kelvin Connection for a Shunt Resistor

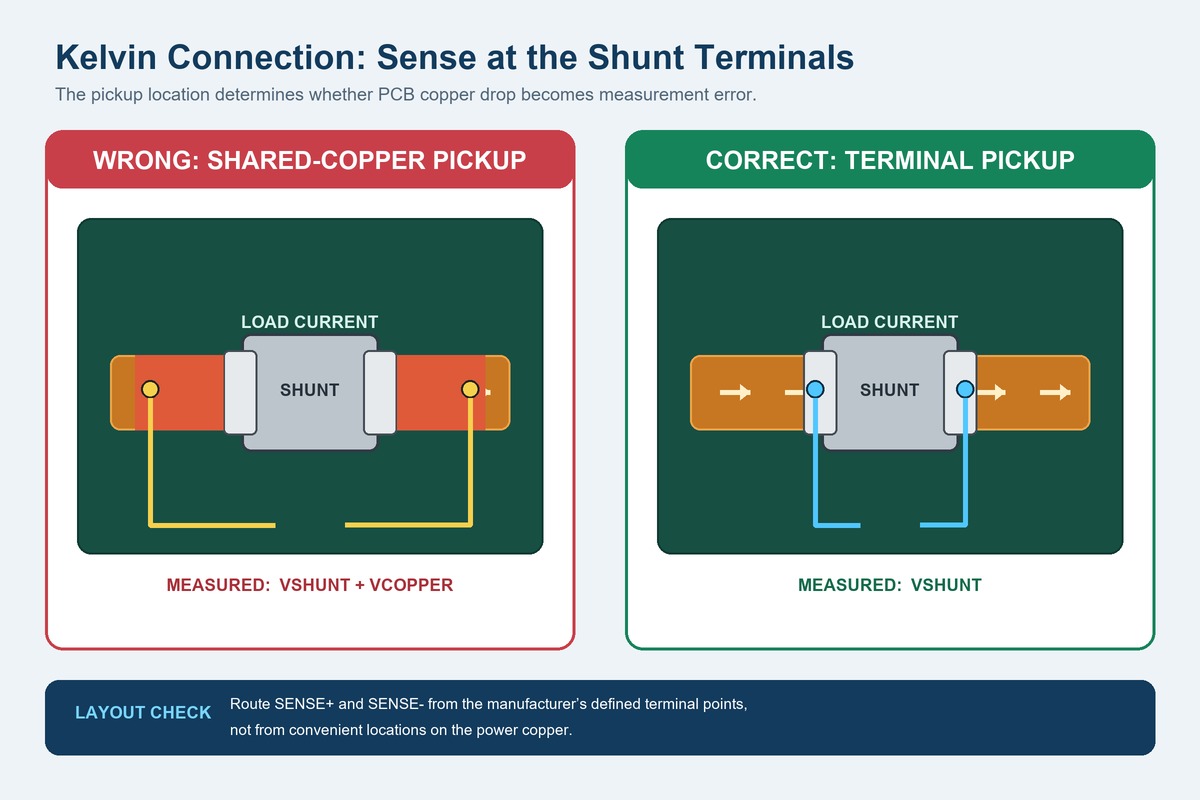
A Kelvin connection separates the voltage-sense path from the high-current path. The two sense traces begin at defined points on the resistor terminals, so voltage drop in the surrounding power copper, vias, pads, and high-current solder path is excluded from the measurement.

Review the layout in this order:

  • Avoid a narrow or asymmetric current entry. Prefer a short, balanced path into both shunt terminals, without unreviewed neck-downs or thermal reliefs.
  • Avoid taking SENSE+ and SENSE- from convenient points on a copper pour. Prefer connections at the terminal locations recommended by the shunt manufacturer.
  • Avoid separating the two sense traces or routing them beside switching nodes. Prefer a close, balanced pair kept away from gate-drive loops and inductors.
  • Avoid sharing sense or reference copper with load-current return. Prefer dedicated low-current paths from the shunt to the amplifier.

For a four-terminal shunt, keep current pads and sense pads distinct. For a two-terminal shunt, pad geometry and trace entry become even more important. A schematic net name does not prove that the physical connection is correct; the copper must be reviewed at the resistor terminals.

Place any approved input filter symmetrically and close to the amplifier. Keep test points on the same nodes used by the measurement circuit. If a fixture measures from different locations, it can pass a board that the product itself reads differently.

A Kelvin error often looks deceptively correct on one prototype. Calibration may remove the error at one current and temperature, but it cannot make changing copper drop disappear across load, temperature, and production variation. If the reading changes when the current path heats, inspect the physical sense-point location before changing calibration constants.

shunt resistor

What Can Distort Current Measurement After Assembly?

Assembly introduces variation that is absent from the schematic. Unequal solder volume can move the effective current-entry point. Poor wetting can increase local resistance. Mechanical stress and board flex can affect the resistor, while heat from nearby components can shift both the shunt and amplifier behavior.

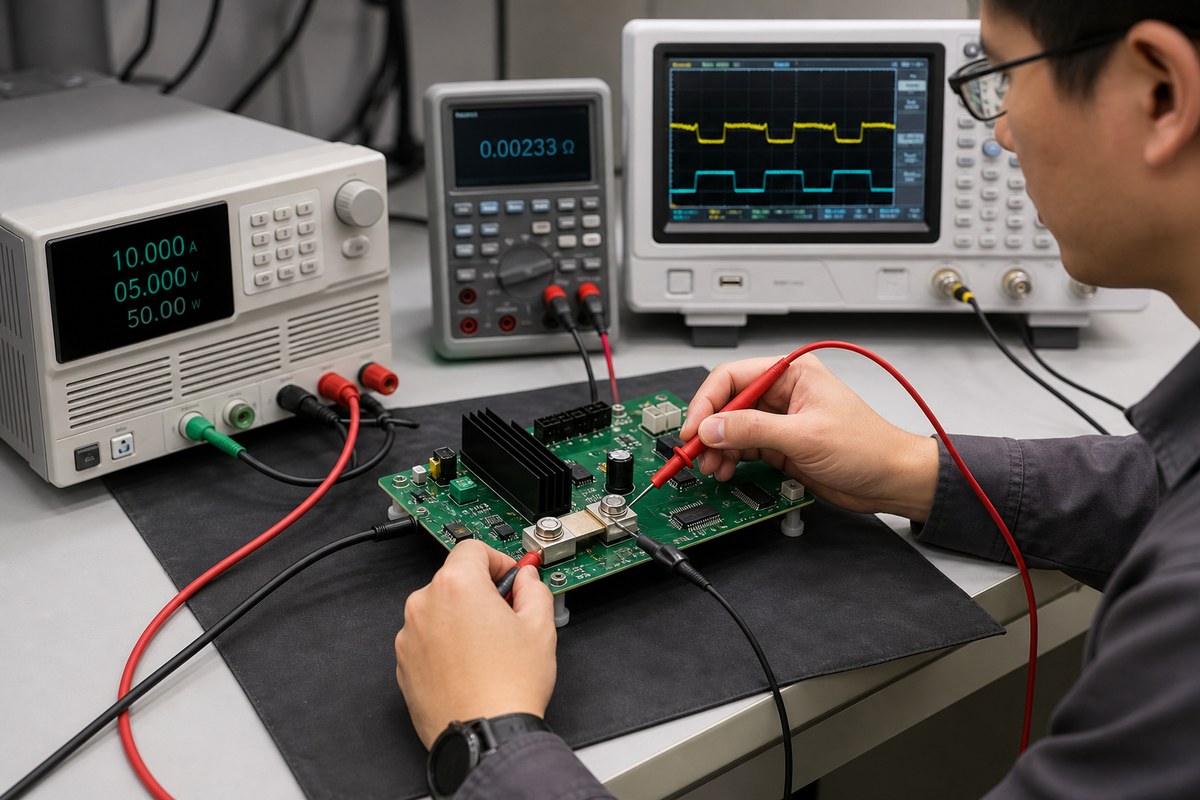
Visible inspection is necessary but not sufficient. AOI can verify component presence and visible solder condition; X-ray can help with hidden connections. Neither proves electrical accuracy. A useful test must specify current, measurement nodes, warm-up or dwell time, temperature condition, acceptance limits, and the result to record.

Use four controls with different purposes:

  • Incoming material — verify the approved manufacturer, part number, lot information, and any required traceability.
  • Assembly workmanship — inspect placement, solder wetting, bridging, contamination, damage, and component seating.
  • PCB implementation — confirm the released current path, Kelvin points, copper construction, and revision were actually built.
  • Electrical acceptance — apply customer-defined current points and verify the measured output, trip behavior, or calibration result within the approved limits.

Example production test plan

  • Test at 10%, 50%, and 100% of the approved operating current.
  • Use the same Kelvin nodes read by the product, not convenient fixture points elsewhere on the power copper.
  • At the high-current point, record the result after the defined warm-up or thermal-stabilization period.
  • Retain input current, shunt voltage, amplifier or ADC output, calculated error, and pass/fail result.

The exact current points and limits must come from the customer’s approved specification; the example shows the level of detail needed for a repeatable test.

Different symptoms suggest different checks: low-current instability calls for noise and offset review; high-current drift calls for thermal review; large board-to-board spread calls for BOM, solder, copper, and fixture comparison. This diagnostic order prevents repeated calibration from hiding a manufacturing problem.

A Shunt Resistor PCB Assembly Example

An ADC current-sensing PCBA project illustrates how an electrical requirement becomes a manufacturing package. The board used four-layer FR-4 with Tg150 material, 2 oz copper on the inner and outer layers, 1.6 mm thickness with ±10% tolerance, and lead-free HASL.

The customer first reviewed the production data and panelization files before fabrication. This created a clear release point: manufacturing preparation could proceed only after the customer confirmed that the production package still represented the intended board.

The SMT build also assigned clear responsibilities:

  • EBest sourced all components, keeping material responsibility with one assembly partner.
  • The boards were separated after SMT and delivered as individual units, so the required delivery format was defined before production.
  • Post-SMT cleaning required the boards to be free of solder balls and other contamination before shipment.

The customer value came from the sequence: define the board construction, approve the production interpretation, assign component responsibility, specify the delivery condition, and make cleanliness an acceptance requirement. Each control removed a different source of ambiguity before shipment.

For a similar project, add the electrical acceptance layer before quotation: the exact shunt part number, approved Kelvin nodes, operating and fault-current range, allowed error, test current points, warm-up condition, and required test record. That gives the manufacturer something objective to build and verify.

The project followed a practical handoff: the customer defined and approved the production interpretation; EBest controlled board construction, sourcing, SMT, separation, and cleanliness; electrical acceptance still required customer-approved current points and limits. That division gives both sides a clear decision before material purchase and a clear acceptance basis before shipment.

What Files Support a Shunt Resistor PCBA Review?

Send one revision-controlled package. At minimum, it should contain Gerber or ODB++ data, fabrication drawing, BOM, pick-and-place file, assembly drawing, and test specification. Mismatched revisions can invalidate an otherwise careful review.

Use each file to answer a specific production question:

  • Fabrication data — What stackup, copper weight, thickness, finish, current-path geometry, and critical dimensions must be built?
  • BOM — Which exact shunt, amplifier, filter components, and approved alternates may be purchased?
  • Assembly data — Where is each part placed, what workmanship or stencil notes apply, and which areas require special inspection?
  • Test specification — Which current is applied, where is voltage measured, how long must the board stabilize, what limits apply, and what evidence is retained?

Also state quantity, prototype or production stage, delivery format, traceability needs, and first-article requirements. For functional testing, provide the fixture interface, power sequence, firmware state, safe operating limits, calibration instructions, and pass/fail criteria.

EBest Circuit can review the manufacturing package, fabricate the PCB, support controlled component sourcing, assemble and inspect the board, and coordinate agreed testing. Circuit architecture, the accuracy budget, safety requirements, and final product validation remain customer-controlled decisions.

Shunt Resistor FAQs

What resistance value should a shunt resistor use?

Start with maximum current and permitted sense voltage, then verify continuous power, transient energy, temperature rise, amplifier range, and the full error budget. There is no universal best resistance value.

Why is a Kelvin connection important for a shunt resistor?

It prevents voltage drop in shared high-current copper and pad paths from being included in the sensed voltage. The smaller the shunt value and signal, the more important the physical sense-point location becomes.

Can a normal resistor replace a current-sense resistor?

Not without review. In a shunt resistor vs normal resistor comparison, nominal resistance alone is not enough. Tolerance, TCR, continuous and pulse ratings, terminal structure, package, land pattern, and thermal behavior must meet the approved requirements.

Can AOI verify shunt resistor accuracy?

No. AOI can verify visible assembly conditions and component presence. Accuracy requires an electrical test with defined current, nodes, temperature or warm-up condition, limits, and records.

What should be sent for a shunt resistor PCBA quotation?

Send controlled PCB data, fabrication drawing, BOM, pick-and-place file, assembly drawing, and test requirements. Include the current range, critical sense points, approved parts, quantity, delivery format, and required records.

Need a Shunt Resistor PCBA Review? Send your PCB data, fabrication drawing, BOM, assembly files, current range, and test requirements to sales@bestpcbs.com. EBest Circuit can review the manufacturing package and help align PCB fabrication, component sourcing, assembly, inspection, and agreed testing before quotation.

You may also like

Digital Potentiometer PCB Guide: Selection and PCBA Checks

August 18th, 2026

A digital potentiometer adjusts resistance through an electronic command instead of a mechanical knob. It is often used for calibration, gain control, sensor trimming, display adjustment, and other settings that need to be changed by a microcontroller.

Choosing one for a PCB involves more than selecting a resistance value. The device must work with the circuit voltage, provide the right resolution, behave correctly when power is turned on, and fit the approved PCB footprint. The assembled board also needs a functional test that confirms the output changes as intended.

This guide explains the information engineers and buyers should check when selecting a digital potentiometer and preparing a board for PCB assembly.

digital potentiometer
Digital potentiometer PCB integration for a compact mixed-signal control board.

What Is a Digital Potentiometer and How Does It Work?

A digital potentiometer, often called a digipot, contains a resistor string and an electronically controlled wiper. A microcontroller changes the wiper position through SPI, I2C, up/down pins, or, in some products, pushbuttons.

The high, low, and wiper terminals resemble the three terminals of a mechanical potentiometer, but they cannot always be used in the same way. They are semiconductor connections with limits on voltage, current, and power. Some devices allow signals only between their supply rails, while others support a wider terminal range. The exact datasheet must be checked before the part is placed in the circuit.

The main specifications include:

  • End-to-end resistance and tolerance
  • Number of taps and step size
  • Linear or logarithmic adjustment
  • Wiper resistance and current limit
  • SPI, I2C, or up/down control
  • Volatile or nonvolatile memory
  • Power-on wiper position
  • Package, pinout, and temperature grade

Use the complete manufacturer part number in the BOM. Parts in the same family may have different resistance values, memory options, interfaces, or packages, even when their abbreviated descriptions look similar.

Digital Potentiometer vs Analog Potentiometer for PCB Design

A mechanical potentiometer keeps its physical wiper position when power is removed. A digital potentiometer may return to a default value or recall a stored setting, depending on the device. This difference can affect how the product behaves during startup.

Design questionDigital potentiometerMechanical potentiometerWhat to check
How is it adjusted?Firmware or digital inputKnob, slider, or trimmerWho needs to change the setting?
What happens at power-up?Default or stored codeWiper stays in positionIs the initial output safe?
What signal can it handle?Limited by IC ratingsLimited by track and contact ratingsCheck actual voltage and current
How is it mounted?Small IC packageMechanical body and mounting hardwareCheck PCB and enclosure space
How is it tested?Send a command and measure the outputMove the wiper and measure the outputDefine the expected result

A digipot is useful when the setting must be controlled remotely, repeated accurately, saved in memory, or adjusted during automatic calibration. A mechanical potentiometer may be better when the circuit must work without power, the user needs direct manual control, or the signal exceeds the ratings of available digital devices.

How to Choose a Digital Variable Resistor

Start with the circuit rather than a distributor search filter. First determine the resistance range, required adjustment resolution, signal voltage, and current through the wiper. Then compare suitable parts using the manufacturer datasheets.

Tolerance deserves particular attention. A device marked 10 kΩ may not provide exactly 10 kΩ from end to end, and the wiper itself adds resistance. The load connected to the wiper can change the output again. If the circuit needs an accurate voltage or gain, calculate the expected range rather than relying only on the nominal resistance.

Also check what happens when the product is switched on. A volatile digipot normally starts at a defined default position and must be set by firmware. A nonvolatile version can recall a saved setting, but its memory has specified write and retention limits.

Before approving the part, confirm:

  • The terminal voltage remains within the datasheet limits during startup, normal use, shutdown, and faults
  • The wiper current and resistor power remain within their ratings
  • The controller supports the required interface and logic voltage
  • The number of taps provides enough adjustment resolution
  • The selected memory behavior suits the product
  • The exact package is available in both prototype and production quantities

These details are more useful in an RFQ than a description such as “10 kΩ digital potentiometer.”

How Does a Digital Potentiometer Circuit Connect to a PCB?

The digital interface and the analog signal path should be reviewed separately. A correct SPI or I2C response only shows that communication is working; it does not show that the analog output is correct.

For SPI, check the clock mode, chip-select timing, data order, maximum clock rate, and reset state. For I2C, check the device address, pull-up voltage, bus loading, and possible address conflicts. Up/down devices need defined direction and step timing.

On the analog side, follow the signal through the high, low, and wiper terminals. Make sure the schematic symbol matches the datasheet pin numbers and that the terminal voltage stays within the permitted range in every power condition. Unused address, reset, write-protect, or shutdown pins should not be left in an undefined state.

Place the recommended decoupling components close to the supply pins. If the wiper carries a sensitive analog signal, keep it away from noisy switching nodes where possible. Test points for the supply, control bus, and wiper output will make prototype debugging and production testing easier.

Digital Potentiometer IC Package and Footprint Checks

The footprint should be checked against the package drawing for the exact ordering code, not against a similar library part. Pay particular attention to whether the manufacturer drawing uses a top or bottom view and how Pin 1 is marked.

Compare the datasheet, schematic symbol, PCB footprint, BOM, pick-and-place data, and assembly drawing. They should agree on:

  • Package name, body size, pitch, and pin count
  • Pin numbering and Pin 1 orientation
  • Pad, solder-mask, and paste dimensions
  • Exposed-pad connection and paste pattern, if present
  • Component height and nearby clearance
  • Moisture sensitivity and storage requirements
digital potentiometer
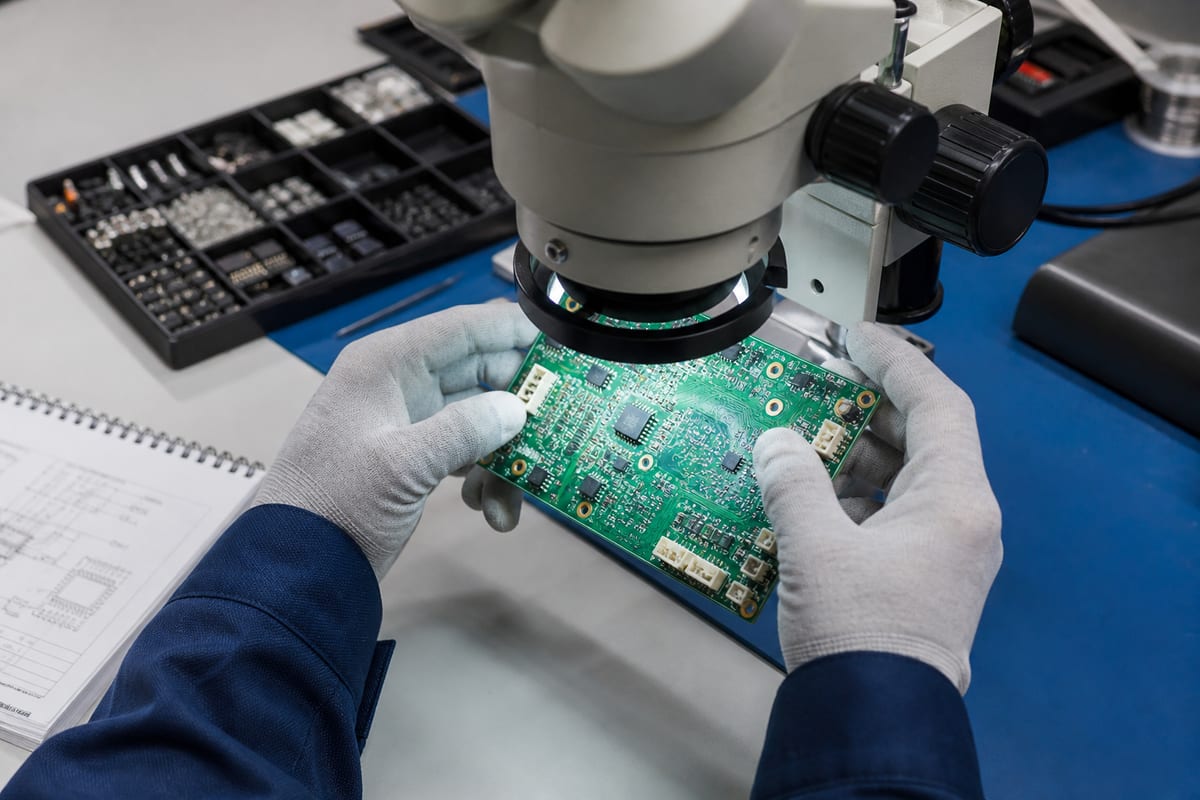
Microscope inspection supports package-orientation and solder-joint checks during PCB assembly.

Small DFN and QFN packages need extra care because most solder joints are hidden under the component. AOI can confirm placement and visible features, but X-ray inspection may be needed to assess hidden joints or an exposed thermal pad. The inspection requirement should be agreed before assembly rather than added after a problem appears.

Digipot BOM, Sourcing, and Substitution Checks

The BOM should list the complete manufacturer part number, not only the resistance and package. It is also helpful to include the interface, number of channels, tap count, memory type, and temperature grade so that purchasing can distinguish between similar versions.

A proposed alternate should be checked for more than pin compatibility. Two parts can fit the same pads but use different commands, start at different wiper positions, or have different limits for terminal voltage and wiper current.

Check an alternate in four areas:

  1. Package: pinout, dimensions, height, and land pattern.
  2. Electrical performance: resistance, tolerance, wiper resistance, voltage, current, bandwidth, and temperature range.
  3. Digital operation: interface timing, address or command format, reset behavior, and memory operation.
  4. Supply status: source, traceability, lifecycle, moisture condition, lead time, and available quantity.

If the alternate requires a firmware change, the updated firmware version should be released with the BOM change. The contract manufacturer can provide sourcing information, but the design owner should approve the replacement before it is used.

Electronic Potentiometer PCBA Inspection and Testing

Assembly inspection and functional testing serve different purposes. AOI can detect many placement, polarity, marking, and visible solder defects. X-ray can provide information about joints hidden under the package. Neither test confirms that the digipot produces the correct analog output when it receives a command.

Possible problemUseful production evidenceInformation needed from the customer
Wrong part or suffixPackage marking and BOM checkApproved MPN and alternates
Wrong orientation or solderingFirst-article inspection, AOI, and X-ray where neededAssembly drawing and acceptance requirements
Wrong startup settingPower-cycle test and initial output measurementRequired startup value and timing
Incorrect adjustmentMinimum, midpoint, and maximum command testsCommands, test points, and output limits
Setting is not retainedWrite, power-off, restart, and readback testRequired memory behavior
digital potentiometer
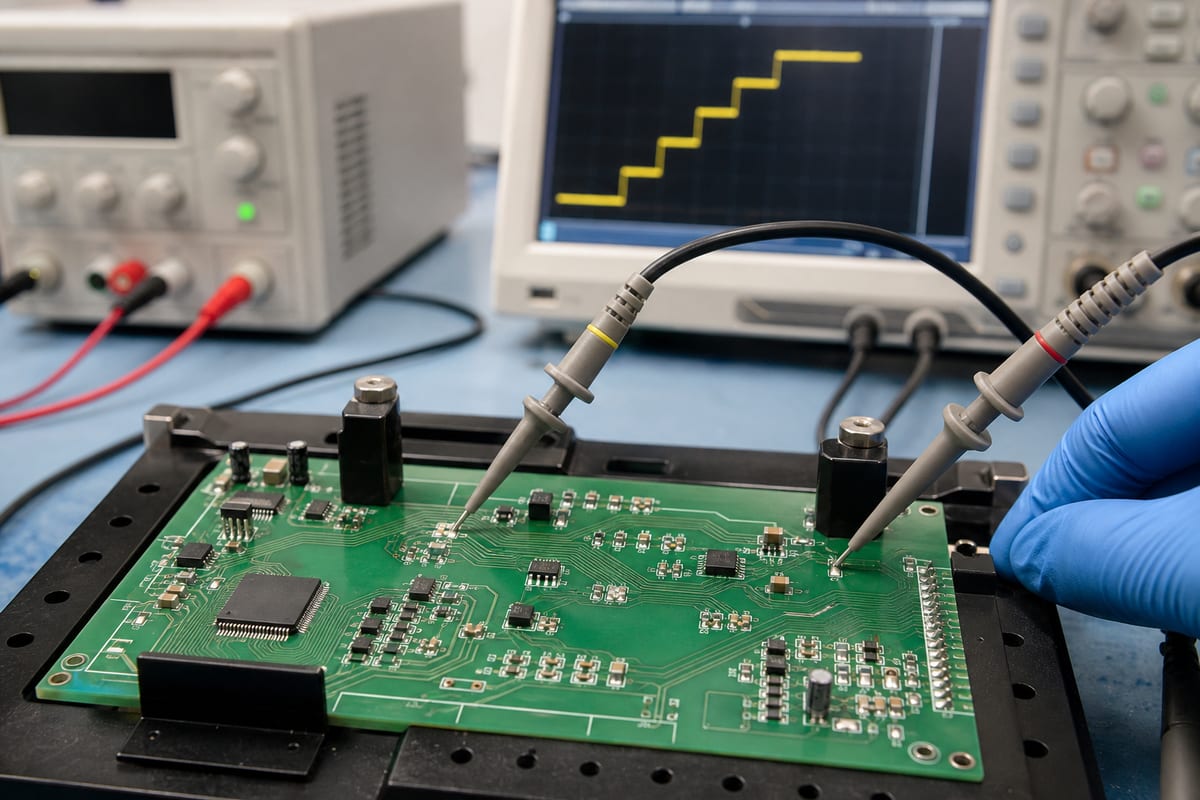
Functional PCBA testing checks whether the commanded wiper settings produce the expected analog output.

A practical test instruction identifies the power supply, connection points, commands, expected outputs, tolerances, and records to keep. Testing three or more wiper positions is usually more informative than checking communication alone. The limits should come from the complete circuit because wiper resistance, loading, temperature, and surrounding components all affect the measured result.

A Digital Potentiometer PCBA Project Example

One customer’s project used a four-layer FR-4 PCB with a finished thickness of 1.6 mm, TG170 material, and 2 oz finished copper on the outer and inner layers. The board had an ENIG finish, blue solder mask, white silkscreen, and a minimum hole-copper requirement of 25 µm.

The customer reviewed the production data before fabrication. The bare PCBs received electrical testing, and the assembly requirements included SMT, AOI, X-ray, test images, board cleaning, individual-board delivery, and antistatic packaging.

The project record does not specify whether a digital potentiometer was fitted. For a digipot on this type of PCBA, the manufacturing package would also need:

  • The BOM and assembly drawing should show the complete part number, package, and Pin 1 orientation.
  • The inspection plan should state whether the package has hidden joints that require X-ray.
  • The functional test should send defined commands and measure the output at minimum, midpoint, and maximum settings.
  • If the setting must survive a power cycle, the test should verify that behavior as well.

These checks confirm three different things: the bare PCB has no opens or shorts, the component is assembled correctly, and the completed circuit responds correctly to the control commands. All three results matter when a digital potentiometer is part of the design.

FAQs About Digital Potentiometer PCB Integration

Can a digital potentiometer directly replace any analog potentiometer?

No. Compare terminal voltage, wiper current, resistance, power, bandwidth, adjustment law, startup state, control method, and package. A circuit that works with a mechanical potentiometer may exceed the limits of a digipot.

Should I choose SPI or I2C for a digital potentiometer?

Choose the interface that fits the controller, available pins, bus architecture, speed, addressing, and firmware. Then check logic levels, pull-ups or chip select, reset behavior, and what happens when one device is unpowered.

Why does the measured output differ from the ideal tap value?

End-to-end tolerance, wiper resistance, loading, temperature, and surrounding components all affect the result. Use a worst-case circuit calculation to set limits, then confirm them on representative assemblies.

What should a digital potentiometer PCBA RFQ include?

Provide the approved PCB fabrication data, BOM with full MPNs, pick-and-place data, assembly drawings, approved alternates, test points, firmware or command requirements, and measurable acceptance limits.

What can EBest Circuit verify?

EBest Circuit (Best Technology) can support component sourcing, DFM review, PCB fabrication, PCBA, inspection, and testing to the requirements supplied with the order. Circuit design, component approval, firmware, and product-specific acceptance limits should be provided or approved by the customer. Send your files to sales@bestpcbs.com for review.

You may also like

How to Choose an IMS PCB Low Volume Manufacturer?

August 18th, 2026

IMS PCB low volume manufacturer services help engineers build and verify thermal boards before committing to higher production quantities. Standard one-layer MCPCB prototypes can be completed in four days under normal service, with 24-hour service available for urgent orders. Copper-base boards, direct thermal path structures, and other custom requirements need an individual schedule.

EBest Circuit (Best Technology) supports IMS PCB prototypes and small batches through PCB fabrication, component sourcing, PCBA, and testing. For an accurate quote, identify the quantity, material, critical dimensions, and expected repeat demand.

IMS PCB low volume manufacturer
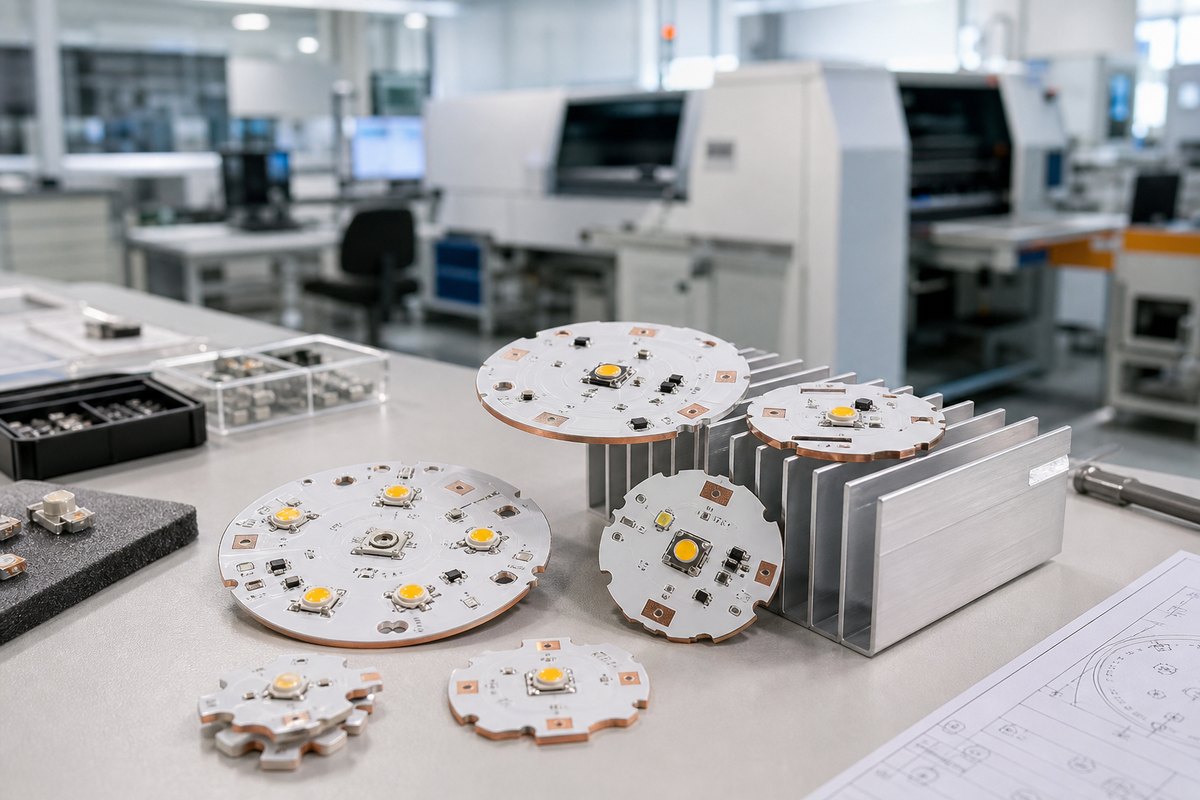
Copper-base IMS PCB samples for a high-power LED module.

What Should You Confirm With an IMS PCB Low Volume Manufacturer?

Ask the manufacturer to answer five questions in writing:

  1. Can you build this exact IMS structure?
  2. Which requirements are standard, and which need material or process confirmation?
  3. When does the quoted lead time start?
  4. Will production files be sent back for approval before fabrication?
  5. Which reports will ship with the boards?

The following lead times apply to standard MCPCB prototypes under 1 m² using standard aluminum, 0.8–2.0 mm board thickness, H/H or 2 oz copper, lead-free HASL, white solder mask, black silkscreen, and 0.8 W/m·K thermal conductivity.

Standard prototype reference Standard service Fastest service
1-layer MCPCB 4 days 24 hours
2-layer MCPCB 14 days 168 hours
4-layer MCPCB 21 days Confirm per project

Custom copper-base or direct thermal path boards require a project-specific schedule. EBest assigns one business contact and three engineering roles covering R&D, PCB process, and PCBA, so commercial and technical questions can be handled together.

Which Insulated Metal Substrate PCB Specs Control Cost and Risk?

The quotation should define the complete thermal stack, not just “aluminum PCB” or “copper IMS.” The metal base spreads heat; the dielectric transfers heat while maintaining electrical insulation.

The most important quotation specifications are:

  • metal-base type and thickness;
  • dielectric thermal conductivity, thickness, and insulation requirement;
  • layer construction and copper weight;
  • finished board thickness and critical mechanical tolerances;
  • surface finish, solder mask, and silkscreen;
  • electrical test and any project-specific report.

Thermal conductivity cannot be compared alone. Dielectric thickness, insulation, operating voltage, heat source, and the heat-sink interface matter together. Copper weight also changes trace geometry and cost: routine inner copper options include 0.5–3 oz, while routine outer copper options include 1–3 oz.

How Does Metal Core PCB Material Choice Affect a Small Batch?

In a low-volume build, material availability and minimum sheet purchases can affect unit cost. Aluminum balances heat spreading, weight, machining, and price. Copper spreads heat more effectively but is heavier and more expensive. Direct thermal path structures are used when the design needs a shorter route from the heat source to the metal base.

Material choice should answer four practical questions:

  • Does it move enough heat for the real operating load?
  • Does the dielectric meet the electrical insulation requirement?
  • Is the selected thickness compatible with the housing and heat sink?
  • Can the same material be obtained for the next build?

Provide both the current quantity and expected repeat demand. This helps engineering assess panel use and purchasing check material continuity. If assembly is required, component sourcing and PCBA are scheduled separately; prototype PCBA can typically be delivered in about 1.5 weeks, subject to BOM and test requirements.

What Files Does an IMS PCB Manufacturer Need for Quotation?

Gerber data defines the circuit pattern, but not always the complete material, mechanical, and inspection requirements. A clear quotation package avoids repeated questions and incorrect assumptions.

A complete bare-board package normally includes:

  • Circuit data: Gerber or ODB++ and NC drill files;
  • Mechanical data: board outline, holes, slots, dimensions, and tolerances;
  • Material data: metal base, dielectric requirement, copper weight, and finished thickness;
  • Finish data: surface finish, solder mask, silkscreen, and marking requirements;
  • Order data: quantity, delivery format, target date, and required reports.

Use the same project name and revision across all files. Conflicting copper, finish, outline, or thickness information can produce an inaccurate quote.

For PCBA, add:

  • BOM with manufacturer part numbers and approved alternatives;
  • pick-and-place data and assembly drawing;
  • polarity and orientation notes;
  • programming and functional-test requirements;
  • special inspection requirements for hidden or high-risk joints.

EBest’s DFM pre-review covers manufacturing data, materials, panelization, component spacing, assembly process, and test access. BOM review can also flag long-lead, obsolete, or alternative components before they delay the build.

Which Checks Reduce Risk in Small-Batch IMS Production?

IMS PCB low volume manufacturer
Electrical testing and batch inspection for copper-base IMS PCBs.

The most useful control is inspection before the remaining value is added.

Before the remaining quantity proceeds, review:

  • material and stack-up confirmation;
  • critical mounting and outline dimensions;
  • electrical-test status;
  • surface finish and solder-mask condition;
  • fit with the heat sink, enclosure, or assembly fixture.

Electrical testing checks continuity and isolation. Required records—such as an electrical test report, COC, or dimensional report—should be agreed before production.

For PCBA, select inspection according to the design. AOI covers visible defects; X-ray is used when joints are hidden beneath packages such as BGA or CSP.

The inspection method should match the defect:

  • SPI: solder-paste volume, area, height, offset, and bridging;
  • First-piece verification: component value, polarity, and placement setup;
  • AOI: visible component and solder-joint defects;
  • X-ray: hidden BGA, CSP, or bottom-terminated joints;
  • Functional test: product behavior against customer-defined limits.

The digital workshop can retrieve key material, batch, cycle, and progress records within five seconds, supporting faster quality investigation.

IMS PCB Case Study: From Prototype to Repeat Order

IMS PCB low volume manufacturer
An engineer checks low-volume IMS PCB prototypes before the repeat order.

A U.S. engineering team was developing a compact high-power LED lighting module. The LEDs generated concentrated heat, so a conventional aluminum IMS board did not provide the heat path required by the mechanical design. The project therefore used a single-sided thermoelectric-separation copper-base PCB.

Project snapshot

  • Application: high-power LED lighting module
  • Customer location: United States
  • Prototype quantity: 10 pcs
  • Repeat order: 500 pcs after prototype validation
  • Sample production lead time: 10 working days
  • Repeat-order production lead time: 15 working days
  • Lead-time basis: production only, counted after material and production-file approval; international shipping excluded

PCB requirements

  • 1.5 mm copper base
  • 3 W/m·K adhesive film, 100 μm thick
  • Pure adhesive lamination not permitted
  • 2 oz copper
  • White solder mask and black silkscreen
  • OSP surface finish
  • Individual-board delivery
  • Production files submitted for customer approval before fabrication
  • COC and electrical test report supplied with shipment

The engineering risk was concentrated in the thermal interface. The 3 W film had to remain 100 μm thick, and pure adhesive could not be substituted because it would create a different thermal and insulation structure. The production data therefore identified the copper-base structure, dielectric film, copper, finish, and delivery format for approval before the first panel was released.

Ten prototype boards were produced in 10 working days. The customer used them to check:

  • LED mounting and polarity;
  • mechanical fit with the module housing;
  • contact between the copper base and heat-spreading surface;
  • temperature behavior during the lighting test;
  • solderability and electrical performance.

After prototype validation, the customer placed a 500-piece repeat order. The approved production revision and material requirements were retained, avoiding another interpretation cycle. Production was completed in 15 working days, and the boards were delivered individually with the agreed COC and electrical test report.

The value of the prototype was not only proving that the circuit worked. It confirmed the material system, thermal interface, manufacturing files, inspection records, and delivery format before the larger order.

How Do You Compare IMS PCB Low Volume Manufacturers?

Compare the answers to these five questions:

Buyer question Strong answer Weak answer
Is my construction understood? The quotation repeats the metal base, dielectric, copper, finish, and delivery format “Standard IMS PCB”
Is the lead time applicable? It states the starting point, material status, fabrication time, and shipment point A fastest-day claim with no conditions
Will engineering review my files? Written DFM questions and production files are returned for approval “Files checked” with no review output
What evidence will I receive? COC, electrical test report, and any project-specific record are named “Quality guaranteed”
Can you support the next stage? Prototype, repeat PCB, sourcing, PCBA, testing, and change control are separated clearly A one-time prototype quote with no continuity plan

EBest operates its own PCB and PCBA factories, works with more than 1,000 supply-chain partners, and holds ISO 9001, ISO 13485, IATF 16949, and AS9100D certifications. Its integrated team supports prototypes, repeat PCB orders, sourcing, assembly, testing, and traceability.

FAQs About IMS PCB Low Volume Manufacturer

Can a standard MCPCB lead time be used for every low-volume IMS board?

No. Published standard lead times apply only under the stated material and process conditions. Copper-base, direct thermal path, special dielectric, unusual finish, tight tolerance, or extra report requirements need project-specific confirmation.

Does EBest Circuit accept prototype and small-batch IMS orders?

Yes. EBest supports prototype and small-batch projects, with the actual quotation based on construction, material availability, quantity, panel use, inspection, and delivery requirements.

What should a manufacturer confirm about an IMS dielectric?

Confirm the material or approved equivalent, thermal conductivity, dielectric thickness, insulation requirement, lamination system, availability, and whether substitution requires written approval.

Why approve production files before fabrication?

Production-file approval lets the customer check how the factory interpreted the stack-up, material, copper, finish, mechanical details, delivery format, and documentation before irreversible work begins.

Should COC and an electrical test report be requested in the RFQ?

Yes, when they are required. Naming them in the RFQ and purchase order makes them controlled shipment deliverables instead of assumptions.

Ready to work with an IMS PCB low volume manufacturer? Send your Gerber files, quantity, metal-base and dielectric requirements, copper weight, finish, critical dimensions, and required reports to sales@bestpcbs.com. EBest’s engineering team will review the project and provide a practical quotation and production plan.

You may also like

Standard Resistor Values: E-Series and BOM Checks

August 18th, 2026

This guide explains how standard resistor values work and how to turn a calculation into a controlled BOM decision. The goal is to reduce sourcing questions, unapproved substitutions, placement errors, and PCBA rework before files reach production.

standard resistor values
Standard resistor values support clearer selection before PCB assembly.

What Are Standard Resistor Values?

Standard resistor values are preferred nominal resistance values arranged in E-series. Instead of manufacturing every possible resistance, suppliers offer repeatable values across each decade, such as 10 Ω, 100 Ω, 1 kΩ, 10 kΩ, and 100 kΩ.

The number after E indicates how many nominal values appear in one decade. E12 contains 12 values, E24 contains 24, and E96 contains 96. A base value repeats by powers of ten, so 4.7 can represent 4.7 Ω, 47 Ω, 470 Ω, 4.7 kΩ, or 47 kΩ.

Before selecting a part, confirm:

  • The acceptable resistance window under worst-case operating conditions.
  • Tolerance and temperature coefficient, not only the nominal value.
  • Package, power rating, working voltage, pulse capability, and technology.
  • A manufacturer part number that is available for the intended production quantity.

A value being standard does not guarantee that every manufacturer offers it in every package or rating. The datasheet and orderable part number remain the final production reference.

Standard Resistor Values Table

The table below lists common base values within one decade. Multiply or divide them by powers of ten to reach the required range. For example, the E24 base value 24 can represent 2.4 Ω, 24 Ω, 240 Ω, 2.4 kΩ, or 24 kΩ.

SeriesValues per decadeCommon tolerance associationBase values
E6620%10, 15, 22, 33, 47, 68
E121210%10, 12, 15, 18, 22, 27, 33, 39, 47, 56, 68, 82
E24245%10, 11, 12, 13, 15, 16, 18, 20, 22, 24, 27, 30, 33, 36, 39, 43, 47, 51, 56, 62, 68, 75, 82, 91
E48482%Finer three-significant-digit spacing
E96961%Finer three-significant-digit spacing
E1921920.5% or tighterVerify the selected product family and datasheet

These tolerance relationships are common associations, not universal purchasing rules. For example, manufacturers also offer many E24 values with 1% tolerance. Always qualify the actual resistor family rather than inferring every specification from the E-series alone.

standard resistor values
Engineers compare E-series options, tolerance, and availability before releasing a resistor part.

E Series Resistors and Tolerance

A denser E-series provides more nominal values within each decade. It helps the selected resistance sit closer to the calculated target, but it does not prove that the full circuit will meet its error budget.

DecisionWhat can go wrongWhat to verify
Use a wider-tolerance partGain, bias, current, or threshold may move outside limits.Worst-case circuit result at both tolerance limits.
Choose a tighter E-seriesThe nominal value is closer, but drift or ratio error may still dominate.TCR, matching, long-term stability, and adjacent component tolerances.
Reduce BOM varietyA convenient common value may not meet the function.Whether the substituted value remains inside the approved electrical window.

For a pull-up or indicator circuit, an E12 or E24 value may provide enough margin. A precision divider, sensor interface, amplifier feedback path, or current-sense circuit may need an E96 value, tighter tolerance, lower TCR, or matched network. The customer engineering team owns the functional limits and released design; the assembly supplier should follow the approved BOM and substitution rules.

E24 Resistor Values for General PCB Assemblies

E24 resistor values offer 24 nominal choices per decade and are widely used where a 5% value provides sufficient circuit margin. The series adds intermediate options such as 11, 13, 16, 20, 24, 30, 36, 43, 51, 62, 75, and 91 that are not present in E12.

E24 is often practical when:

  • The function is tolerant of modest resistance variation.
  • The value is used for non-critical bias, indication, damping, or ordinary pull-up and pull-down duties.
  • Cost, availability, and lower BOM variety matter more than very fine nominal spacing.
  • Worst-case calculations confirm that the chosen value and tolerance are safe.

Do not use the application name alone to approve a resistor. A 330 Ω part may work for one LED circuit but overdrive or underdrive another because supply voltage, LED forward voltage, and target current differ. Calculate the function first, then select the E24 value that keeps the full operating range within limits.

E96 Resistor Values for Precision Circuits

E96 resistor values provide 96 nominal choices per decade and are commonly associated with 1% resistors. Their three-significant-digit spacing supports closer selection for analog feedback, sensing, precision division, filtering, and control functions.

E96 base values (100–976 within one decade)
100, 102, 105, 107, 110, 113, 115, 118, 121, 124, 127, 130
133, 137, 140, 143, 147, 150, 154, 158, 162, 165, 169, 174
178, 182, 187, 191, 196, 200, 205, 210, 215, 221, 226, 232
237, 243, 249, 255, 261, 267, 274, 280, 287, 294, 301, 309
316, 324, 332, 340, 348, 357, 365, 374, 383, 392, 402, 412
422, 432, 442, 453, 464, 475, 487, 499, 511, 523, 536, 549
562, 576, 590, 604, 619, 634, 649, 665, 681, 698, 715, 732
750, 768, 787, 806, 825, 845, 866, 887, 909, 931, 953, 976

Move the decimal point to reach the required decade: 487 can represent 48.7 Ω, 487 Ω, 4.87 kΩ, or 48.7 kΩ. Before releasing an E96 part, confirm whether absolute tolerance, resistor ratio, TCR, thermal gradients, noise, or long-term drift controls the real accuracy.

A tighter nominal value can also increase sourcing constraints. When alternates are allowed, define the acceptable resistance, tolerance, TCR, package, power, voltage, technology, and qualification requirements rather than approving ‘same value’ substitutions.

How to Find the Nearest Standard Resistor Value

The nearest numerical value is not automatically the safest production choice. The correct direction depends on what failure must be prevented. A higher resistance may reduce LED current, but it may also slow a pull-up edge or change amplifier gain.

Use this selection sequence:

  1. Calculate the ideal resistance using worst-case supply, load, temperature, and component limits.
  2. Define the minimum and maximum resistance that keep the circuit inside its approved operating window.
  3. Select the appropriate E-series and identify the nearest lower and higher standard values.
  4. Apply resistor tolerance to both candidates and repeat the worst-case calculation.
  5. Verify power dissipation, derating, working voltage, pulse energy, TCR, package, footprint, and availability.
  6. Release one exact manufacturer part number and document the approved alternate criteria.

Example: an LED calculation produces 193 Ω. Possible preferred values include 180 Ω and 200 Ω in E24, or 191 Ω and 196 Ω in E96. If excess current is the main risk, the higher value may provide more margin, but brightness and minimum-current requirements must still be checked. The calculation, not the lookup table, approves the part.

Standard SMD Resistor Values for PCBA

Standard SMD resistor values follow the same preferred E-series used by through-hole resistors. Package size changes assembly and electrical limits; it does not create a separate nominal-value system.

A BOM line that says only ’10 kΩ resistor’ leaves too many production decisions unresolved. A sourcing team may find many 10 kΩ parts with different tolerance, size, power, working voltage, TCR, pulse rating, construction, termination, lifecycle status, and price.

A production-ready resistor BOM line should confirm:

  • Nominal resistance with an unambiguous unit, such as 4.7 kΩ rather than 4.7.
  • Tolerance, package, power rating, and maximum working voltage.
  • TCR, pulse capability, current-sense construction, or other function-specific limits when relevant.
  • Manufacturer name, exact manufacturer part number, and lifecycle status.
  • Approved alternates or a clear no-substitution instruction.
  • Footprint, pick-and-place data, polarity rules where applicable, and assembly drawing consistency.

Very small SMD resistors may have no readable top marking. Reel labels, incoming inspection, feeder setup, material traceability, automated optical inspection, and electrical test requirements therefore matter more than visual identification alone.

standard resistor values
BOM, reel, footprint, and inspection checks help prevent wrong-value SMD resistor substitutions.

EBest Circuit (Best Technology) can support PCB fabrication, BOM and component sourcing review, SMT or through-hole assembly, inspection, and agreed testing coordination within the released project scope. The customer retains responsibility for circuit function, tolerance limits, approved substitutions, firmware, certification, and final product validation.

FAQ About Standard Resistor Values

1. What are the most common standard resistor values?

Common examples include 10 Ω, 22 Ω, 47 Ω, 100 Ω, 220 Ω, 330 Ω, 470 Ω, 1 kΩ, 2.2 kΩ, 4.7 kΩ, 10 kΩ, 47 kΩ, and 100 kΩ. Their popularity does not make them correct for every circuit.

2. What is the difference between E12, E24, and E96?

E12 has 12 nominal values per decade, E24 has 24, and E96 has 96. A denser series gives more choices, but tolerance, TCR, power, voltage, package, and availability still need separate confirmation.

3. Are 1% resistors always E96 values?

No. E96 is commonly associated with 1% tolerance, but tolerance and nominal-value series are separate specifications. Many E24 values are also available as 1% parts.

4. Can I always choose the nearest standard resistor value?

No. Compare both the lower and higher candidates under worst-case circuit conditions. The safe direction depends on whether the function controls current, gain, timing, bias, threshold, damping, or another parameter.

5. Are standard SMD resistor values different from through-hole values?

They use the same preferred-value concept. The available resistance range and electrical limits vary by package, resistor technology, tolerance, power, voltage, and manufacturer.

Ready to move your resistor-controlled PCB assembly into production? Send your Gerber files, controlled BOM, pick-and-place data, assembly drawings, quantity, approved substitution rules, and test requirements to sales@bestpcbs.com. EBest Circuit (Best Technology) will review the package for PCB fabrication and PCBA quotation, helping you identify unclear resistor specifications before sourcing and assembly.

You may also like

Standard Copper Busbar Sizes: A Buyer’s Selection Guide

August 17th, 2026

Standard copper busbar sizes can shorten sourcing time, but width and thickness alone do not make a part safe or ready to build. If material, current conditions, hole pattern, finish, and tolerances are unclear, the result may be overheating, poor terminal alignment, enclosure interference, or a quotation based on the wrong part.

This matters when the busbar connects to a PCB, terminals, or an assembled power module. A small dimension change can affect mounting holes, clearances, tool access, and the assembly sequence. If you send us the released busbar drawing and PCB files, the EBest Circuit (Best Technology) team can review the manufacturing interfaces together, point out missing quotation details, and help you define a practical PCB/PCBA, inspection, and testing scope. Your engineers keep control of the electrical design and final approval; our role is to make the handoff easier and reduce avoidable surprises before production.

Standard copper busbar sizes

Standard Copper Busbar Sizes in mm and Inches

There is no single worldwide list of standard copper busbar sizes. In practice, “standard” usually means a size regularly stocked by a mill, distributor, or fabricator. Availability varies by region, copper grade, temper, length, quantity, and supplier.

Metric tables commonly show width × thickness, such as 40 × 5 mm. North American tables may show thickness × width, such as 1/4 × 2 in. Always label both dimensions and units on the drawing; an unlabeled pair can be reversed during quotation or manufacturing.

Common reference thicknesses include:

  • Metric: 3, 5, 6, 8, and 10 mm.
  • Imperial: 1/16, 1/8, 3/16, 1/4, 3/8, and 1/2 in.
  • Larger or unusual combinations may require plate cutting or a custom material order.

ASTM B187/B187M covers requirements for copper bar, bus bar, rod, and shapes and lists several copper UNS designations for electrical applications. It is a material specification, not a universal stock catalogue. The purchase order and released drawing still need the copper grade, dimensions, tolerances, finish, and any certificate requirements.

Buyer check: Confirm the exact stock form with the proposed supplier before freezing the design. A size shown online may not be available in the required grade, length, or quantity.

Standard Copper Busbar Sizes Chart

This chart is a dimensional reference, not an ampacity table. The combinations are common examples, but they are not a promise of supplier availability.

Nominal width × thickness Cross-sectional area Approximate inch equivalent Confirm before release
20 × 3 mm 60 mm² 0.787 × 0.118 in. Grade, length, cutting tolerance
25 × 3 mm 75 mm² 0.984 × 0.118 in. Width/thickness order
30 × 3 mm 90 mm² 1.181 × 0.118 in. Edge condition and flatness
40 × 5 mm 200 mm² 1.575 × 0.197 in. Hole clearance and bends
50 × 5 mm 250 mm² 1.969 × 0.197 in. Finish and contact areas
60 × 5 mm 300 mm² 2.362 × 0.197 in. Length and assembly envelope
80 × 10 mm 800 mm² 3.150 × 0.394 in. Support, hardware, tooling
100 × 10 mm 1,000 mm² 3.937 × 0.394 in. Enclosure space and tolerances

Cross-sectional area equals width multiplied by thickness, but equal area does not guarantee equal performance. Shape also affects surface area, stiffness, bending, connection geometry, AC effects, and heat dissipation.

Do not silently replace a metric size with the nearest inch fraction. For example, 5 mm and 3/16 in. are close but not identical. The difference can affect holes, bends, stack height, terminal alignment, and clearances. Record every approved alternative on the controlled drawing.

How to Select Busbar Size?

Start with the customer’s validated electrical and mechanical requirements, then compare those requirements with real stock availability.

Electrical inputs:

  • Continuous, peak, and fault current.
  • AC frequency or DC operation.
  • Ambient temperature and permitted temperature rise.
  • Enclosure, ventilation, bar spacing, orientation, and parallel bars.
  • Joint design, plating, allowed voltage drop, and protection strategy.

Mechanical and integration inputs:

  • Space around the PCB, terminals, enclosure, and other conductors.
  • Holes, slots, bends, datums, and critical tolerances.
  • Supports, vibration, weight, and installation sequence.
  • Finish, masking, insulation, and contact areas.

If a stocked size meets the released requirements, it may reduce lead time and waste. If it does not, use a controlled custom route instead of weakening clearances, joints, or mechanical requirements to fit a catalogue bar.

Standard copper busbar sizes

How Copper Busbar Size and Current Rating Relate

Copper busbar size and current rating are related, but there is no universal conversion from cross-sectional area to allowable current. A published value is valid only under its stated conditions.

The Copper Development Association’s rectangular-busbar data shows that temperature rise, surface emissivity, number of bars, spacing, and configuration can change ampacity. Enclosure and ventilation conditions also influence temperature rise. A bare bar in open air should not inherit the same current rating when it is enclosed, coated, stacked, or connected through poorly controlled joints.

Before accepting a current value, confirm:

  • The source table, standard, calculation, or test report.
  • Copper grade, dimensions, orientation, and surface condition.
  • Ambient temperature and permitted temperature rise.
  • AC/DC conditions, frequency, spacing, parallel bars, and enclosure.
  • Joint design, terminal limits, protection, and validation method.

A size chart can narrow the options; it cannot approve the final conductor. The customer releases the rating and acceptance criteria. A useful manufacturing review then checks whether the received drawing, PCB interface, controlled dimensions, and proposed inspection or test evidence agree with that release.

Copper Bus Bar Stock or Custom Size?

Standard copper bus bar stock can reduce sourcing time when its grade, dimensions, and tolerances match the released part. A custom route is more suitable when the approved envelope, terminal geometry, bends, hole pattern, or current path cannot be met without risky substitutions.

Use stock when:

  • The exact grade, condition, length, and certificates are available.
  • Dimensions and tolerances meet the drawing.
  • Cutting, drilling, forming, and finishing have enough process margin.
  • The size does not force changes to clearances, joints, or enclosure space.

Consider custom material or fabrication when:

  • Stock would create excessive machining or waste.
  • A special thickness, profile, bend, or controlled edge is required.
  • Hole patterns and interfaces have little tolerance with the nearest stock size.
  • Validation depends on the exact released cross-section.

Project example: A buyer selects a 50 × 5 mm bar because its 250 mm² area fits an early calculation. During integration review, it blocks connector tool access and leaves too little space around an offset terminal. Changing to a narrower, thicker bar may solve the space problem but alter bending, cooling, and joint geometry. The safer next step is to compare validated options, update the mechanical stack, and release one controlled drawing before quotation.

Why integrated review matters: A busbar and PCB can each pass an isolated drawing check and still fail together. Hole patterns must align; bends and thickness must fit the enclosure; contact areas must match the assembly process; and installers need access for hardware, soldering, inspection, and rework.

How EBest Circuit supports the handoff: Our team can review the released busbar and PCB manufacturing interfaces in one quotation package, then connect that review with PCB fabrication, component-sourcing support, PCBA, inspection planning, and agreed testing coordination. We will flag unclear inputs and state the proposed scope instead of quietly making design assumptions. This gives your team a clearer decision record while electrical design, system safety, and final approval remain under your control.

Send these RFQ files:

  • Released 2D drawing and a matching 3D model when the part is formed.
  • Material, finish, masking, certificate, and quantity requirements.
  • Critical dimensions, datums, tolerances, and inspection expectations.
  • Customer-approved ratings, test inputs, and acceptance limits.
  • PCB files, BOM, assembly interfaces, revision, and delivery target.

Send the controlled package, not a screenshot of a size table. Email the files and required scope to sales@bestpcbs.com; our team will review what is ready, identify what still needs confirmation, and help you define the next manufacturing step.

North American Charging Equipment PCB and Busbar Project

Standard copper busbar sizes

A North American customer needed 500 PCBs for charging equipment within a one-week lead time. EBest Circuit manufactured and delivered the order to these released PCB requirements:

  • 2-layer FR-4 with Tg 130°C.
  • 1 oz finished copper and 1.6 mm finished board thickness.
  • Green solder mask and white silkscreen.
  • HASL surface finish.
  • Routed and delivered as individual boards rather than panels.

The board was used in a charging-equipment assembly with a rectangular copper busbar interface. The customer’s drawings controlled the busbar width, thickness, copper grade, finish, and current rating; the PCB’s 1 oz copper was not treated as the main current path.

To meet the one-week schedule, our team checked the PCB stack-up, drill and outline data, individual-board routing, busbar mounting holes, terminal geometry, electrical clearances, and fastener access under one revision. The 500 boards were fabricated, routed, inspected, and packed as individual pieces.

This case shows the value of sending the PCB files and controlled busbar drawing together. EBest Circuit can review the interfaces, produce the PCB, and support sourcing and PCBA when required, while the customer retains control of electrical ratings and final design approval.

FAQs About Standard Copper Busbar Sizes

Is there one universal list of standard copper busbar sizes?

No. “Standard” usually reflects recurring supplier stock. Available combinations differ by region, grade, thickness, temper, and quantity, so confirm availability before release.

Should dimensions be written as width × thickness?

Metric tables often use width × thickness, while some imperial references list thickness × width. Label the dimensions and units on the drawing to prevent reversal.

Can two bars with the same cross-sectional area carry the same current?

Not automatically. Shape, orientation, enclosure, temperature rise, spacing, joints, and surface condition can change performance. Validate the actual assembly.

Is C11000 the only copper grade used for busbars?

No. C11000 is common, but ASTM B187/B187M lists several copper UNS designations for electrical applications. Specify the required grade or approved alternatives.

What should be sent with a copper busbar RFQ?

Send the released drawing, material and finish, quantities, tolerances, inspection needs, approved ratings, assembly interfaces, revision, and delivery target.

If your busbar must align with a PCB, terminals, enclosure, or power assembly, we would be glad to look at the manufacturing package with you. Send the released files, BOM, quantities, and acceptance requirements to sales@bestpcbs.com. The EBest Circuit (Best Technology) team will point out missing quotation inputs and help define a practical PCB/PCBA, inspection, and agreed testing scope before production.

Use this guide to review Standard copper busbar sizes, then send your released PCB, busbar, BOM, quantity, and acceptance requirements to sales@bestpcbs.com.

You may also like

Copper Thermal Conductivity vs Temperature for PCB Design

August 17th, 2026

Copper thermal conductivity vs temperature data can look precise while still producing the wrong PCB decision. The commonly quoted room-temperature value describes bulk copper under defined conditions; it does not automatically represent a finished board, a plated feature, or the complete component-to-cooler heat path.

PCB buyers therefore need to confirm the copper temperature and condition, the released stackup and heat-spreading geometry, and the drawings, fabrication limits, and test inputs required before production. This guide turns reference conductivity data into concise, manufacturable PCB checks.

Copper thermal conductivity vs temperature
Copper thermal conductivity vs temperature review at a PCB thermal-analysis bench.

Copper Thermal Conductivity vs Temperature Chart

Copper is often assigned a single thermal conductivity value, but that shortcut can mislead a PCB thermal review. The value depends on temperature, material condition, and purity. It also describes bulk copper—not the effective thermal conductivity of a finished multilayer board.

The table below is a practical reference for pure copper from 100 K to 1,200 K. It shows the expected downward trend as temperature rises through the range relevant to many industrial calculations.

Temperature (K)Approx. temperature (°C)Thermal conductivity k (W/m·K)
100-173480
150-123429
200-73413
250-23406
30027401
400127393
600327379
800527366
1,000727352
1,200927339

For an ordinary PCB operating near room temperature, 401 W/m·K is a reasonable first-pass value for bulk copper. For a high-temperature calculation, use a value matched to the expected copper temperature—not the ambient air temperature—and retain margin for interfaces and manufacturing variation.

Copper Thermal Conductivity Temperature Dependence Explained

In copper, mobile electrons carry most of the heat. As temperature rises, atomic vibrations increase and scatter those electrons more frequently. The result is lower thermal conductivity across the normal and elevated-temperature range.

The behavior is not one simple straight line across every temperature. At cryogenic temperatures, conductivity can rise sharply to a peak and then fall again near absolute zero. The peak is highly sensitive to purity and defects, so a room-temperature copper value cannot be extended into a cryogenic model.

  • Temperature range: State the minimum, normal, and maximum copper temperature used in the calculation.
  • Copper condition: Identify the relevant copper grade, temper, plating, and any alloyed or bonded layers.
  • Heat-flow direction: Separate in-plane spreading through copper from through-board heat flow across dielectric layers.
  • Boundary conditions: Define the heat source, contact area, cooling interface, airflow, and allowed temperature rise.

A useful supplier question is not only “What is copper’s k value?” It is “Which value and temperature range were used in the thermal model, and does the released stackup support that heat path?”

Thermal Conductivity of Copper at Various Temperatures

Published datasets agree on the broad room-to-high-temperature trend: copper is near 400 W/m·K around room temperature and gradually declines as temperature rises. One Zenodo dataset lists 401 W/m·K at 273 K, 398 W/m·K at 300 K, 392 W/m·K at 400 K, and 383 W/m·K at 600 K.

Cryogenic data require more care. NIST publishes OFHC copper curve fits from 4 K to 300 K for several residual resistance ratio (RRR) values. RRR is a practical indicator of purity and defect scattering; higher-RRR copper can reach a much larger low-temperature conductivity peak than ordinary copper.

  • Room and elevated temperatures: Use a temperature-matched value and document the source.
  • Cryogenic service: Specify the copper grade and an appropriate RRR assumption or material certificate.
  • Wide operating range: Use a curve or temperature bands instead of one constant value.
  • Production release: Keep the thermal-model assumption aligned with the copper actually purchased and fabricated.

For PCB purchasing, do not request “high-purity copper” as an undefined phrase. Put the required copper specification, thickness, finished-copper tolerance, surface finish, and any evidence requirement into the drawing or procurement package.

What Is the Thermal Conductivity of Copper at Room Temperature?

At approximately 20-27°C, pure copper is commonly treated as about 400-401 W/m·K. That number is useful for material comparison and early thermal estimates, but it should not be copied directly into a board-level claim.

A PCB contains copper foils, plated holes, resin, glass reinforcement, solder mask, surface finish, solder, components, and interfaces. The copper may spread heat efficiently along the plane of a layer, while through-thickness heat transfer is restricted by dielectric materials and small contact areas.

  • Use 401 W/m·K: For a documented first-pass bulk-copper estimate near room temperature.
  • Use a lower temperature-specific value: When copper operates well above room temperature.
  • Use effective PCB properties: When modeling the complete stackup or through-board heat flow.
  • Use test correlation: When temperature limits are tight, interfaces dominate, or safety/reliability depends on the prediction.

Before RFQ, the customer should identify whether the value applies to raw copper, a copper feature, one PCB layer, or the assembled thermal path. This prevents a material constant from becoming an unsupported finished-product requirement.

Copper Conductivity vs Temperature for PCB Heat Spreading

Temperature-dependent copper conductivity matters, but geometry usually controls whether the available copper can move enough heat. A thin trace and a wide copper plane can use the same material value while producing very different temperature rises.

  • Copper thickness and area: Confirm base copper, finished copper, plating contribution, plane coverage, neck-downs, and current/heat bottlenecks.
  • Layer location: Identify whether the principal heat-spreading layer is external or buried and what dielectric separates it from the source.
  • Thermal vias: Define finished hole size, plating, quantity, pitch, fill/cap requirements, and the receiving copper area.
  • Interfaces: Include solder joints, thermal pads, dielectric layers, coatings, mounting pressure, and contact resistance in the model.
  • Manufacturing tolerances: Review whether minimum feature sizes, annular rings, registration, copper balance, and finished thickness can support the proposed heat path.

EBest Circuit (Best Technology) can review the released PCB data for manufacturability, stackup, copper distribution, via structures, fabrication, assembly, inspection, and test coordination. The customer remains responsible for system heat loads, component junction limits, airflow, enclosure cooling, and final product validation unless a separate scope is agreed.

Copper thermal conductivity vs temperature
PCB copper heat-spreading measurement with probes and thermal imaging.

Copper Thermal Conductivity vs Aluminum for PCB Tradeoffs

At room temperature, copper conducts heat substantially better than aluminum: approximately 401 W/m·K versus about 237 W/m·K for pure aluminum. Copper can therefore move more heat through the same idealized cross-section, but conductivity alone does not select the best PCB construction.

Decision factorCopperAluminum-base option
Thermal conductivityAbout 401 W/m·KAbout 237 W/m·K
WeightHeavierLighter
PCB roleFoil, planes, and viasMetal-core base
Buyer checkCopper geometryDielectric and base

Choose the construction by the complete heat path, electrical isolation, weight, mechanical needs, achievable geometry, cost, and validation plan. A copper-heavy FR-4 board, an MCPCB, and a ceramic PCB solve different constraints; none should be selected from one W/m·K number alone.

PCB Project Example: Copper Thermal Conductivity in Heat-Spreading Checks

In one customer order, EBest Circuit reviewed a compact 47 × 34.5 mm, 12-layer FR-4 TG180 PCB built to IPC Class 3. The build combined blind vias from L1-L2 and L12-L11, buried vias from L2-L11, resin-plugged and plated-flat vias, a 2.0 mm finished thickness, and ENIG. Before production, the customer required the production stackup and CAM artwork for approval.

The thermal and manufacturing concern was not selecting another handbook conductivity value. The order data did not confirm the proposed 1 oz outer copper, while the residual copper area differed significantly among layers. Those details affect the real heat-spreading geometry, copper balance, and buildability even though bulk copper near room temperature remains about 401 W/m·K.

  • Outer-copper clarification: The customer had not confirmed 1 oz outer copper. EBest Circuit therefore kept it open in the EQ and production stackup instead of treating it as an approved input.
  • Via feasibility: The blind/buried sequence and resin-plugged, plated-flat vias required manufacturing review. The customer retained a ±2 mil via tolerance, so the released drawing and inspection basis had to preserve that decision.
  • Test-coupon confirmation: The COC mentioned a test coupon, but this order did not include impedance control. The customer confirmed that no coupon was needed, so the production documents were aligned with the agreed scope.
  • Copper balance decision: Because residual copper differed substantially by layer, engineering recommended a 1.0% bow-and-twist control. The customer did not accept the recommendation, so the decision was recorded and the production data remained customer-controlled.
  • Release gate: EBest Circuit issued the production stackup and CAM artwork for customer approval. Production could begin only after those documents were confirmed.

This order shows why copper thermal conductivity must be checked together with the actual stackup and released copper geometry. The credible supplier action was to surface unresolved data, preserve the customer's decisions, and gate production on approved manufacturing documents—not to claim that the 401 W/m·K material value alone guaranteed board temperature.

Copper thermal conductivity vs temperature
Production stackup and CAM review before releasing a 12-layer PCB order.

Copper Thermal Conductivity vs Temperature FAQs

Does copper thermal conductivity decrease as temperature increases?

Across typical room and elevated-temperature ranges, yes. Reference tables show a gradual decline as temperature rises. Cryogenic behavior is different and depends strongly on purity and RRR.

What copper thermal conductivity value should I use at room temperature?

About 400-401 W/m·K is a common bulk-copper reference near 20-27°C. State the source and do not treat it as the effective conductivity of the complete PCB.

Can I use one copper conductivity value for the full PCB temperature range?

Only for a rough model over a narrow range with adequate margin. For wide or critical ranges, use temperature-dependent data or defined temperature bands and correlate the model with testing.

Does thicker copper automatically solve a PCB hotspot?

No. Thickness can help, but plane area, bottlenecks, layer position, vias, dielectric interfaces, component attachment, and cooling boundary conditions also control the result.

What should I send for a PCB thermal and DFM review?

Send the controlled fabrication data, stackup, finished-copper requirements, drill data, BOM and placement data for assembly, expected operating range, heat-source information, thermal-interface assumptions, and the temperatures or test points that must be verified.

For a copper thermal conductivity vs temperature manufacturability review, contact EBest Circuit (Best Technology) at sales@bestpcbs.com with the controlled board package and operating assumptions. The review can then focus on the files, tolerances, heat-spreading features, and verification inputs that affect fabrication and assembly risk.

You may also like

USB Motherboard Pinout: Header Types and PCB Checks

August 17th, 2026

USB motherboard pinout errors can damage a port, prevent device enumeration, or force a board respin. Common causes include a reversed connector view, incorrect footprint, swapped differential pair, missing protection, or an uncontrolled assembly drawing.

This guide compares common internal USB headers and the checks needed before PCB fabrication and assembly. Always follow the released motherboard manual, connector drawing, USB specification, and customer-approved electrical design.

USB motherboard pinout
A keyed internal USB motherboard header checked before PCB fabrication and assembly.

What a USB Motherboard Pinout Shows

A USB motherboard pinout maps each header position to power, ground, USB 2.0 data, SuperSpeed pairs, sideband, shield, key, or no-connect functions.

Confirm the drawing view before comparing signals. Pin 1, row numbering, key position, and latch direction must agree across the schematic, footprint, assembly drawing, cable drawing, and inspection record.

Before approving a pinout, confirm four things:

  • The exact connector part number and its manufacturer drawing.
  • The viewing direction used by every pin-number diagram.
  • The signal-to-pin mapping in the released schematic and netlist.
  • The mating cable or front-panel assembly, including any proprietary wiring.

Matching pin counts do not prove matching assignments. OEM and custom boards may use proprietary keying or pin maps.

USB Motherboard Connector Types

USB generation and mechanical header type are separate decisions. USB 2.0, USB 3.x, and front-panel Type-C headers use different connectors and signal sets.

Header typeTypical formMain signalsBuyer check
USB 2.0 internal header2 x 5 positions, commonly one key/missing pinTwo USB 2.0 ports: power, D-, D+, groundConfirm key position and whether pin 10 is NC, shield, or overcurrent-related.
USB 3.x front-panel headerShrouded 19/20-position familyUSB 2.0 lines plus SuperSpeed TX/RX pairs, power, groundConfirm connector revision, pair polarity, pair naming, and mating cable.
Front-panel USB Type-C headerCompact Type-E/Key-A style familyHigh-speed lanes and control/sideband functions depend on implementationConfirm the exact standard revision, connector drawing, orientation, and controller architecture.

An adapter may solve a mechanical mismatch, but it does not confirm bandwidth, power, controller support, or pin assignment.

USB 2.0 Header Pinout and Keying

A common USB 2.0 header serves two ports, each using +5 V, D-, D+, and ground. A missing pin or blocked cavity provides keying; the remaining position may be NC, shield, or overcurrent-related.

An incorrect USB 2.0 connection can cause several different outcomes:

  • VBUS applied to a data or ground position can damage the port or connected device.
  • D+ and D- swapped within a port can prevent enumeration or create intermittent behavior.
  • A connector installed in the wrong orientation can defeat the intended protection of the missing key pin.

For a new PCB, verify pin 1, key location, footprint orientation, courtyard, housing clearance, solder mask, and assembly notes. For an existing board, use its exact manual and revision.

USB 3.0 Header Signals and Pair Routing

A USB 3.0 front-panel header combines USB 2.0 signals with SuperSpeed TX/RX pairs, power, ground, and shield or drain connections. More signals make routing and documentation errors more costly.

TX/RX labels can appear reversed when drawings describe opposite sides of the interface. Confirm the naming convention and connector view before changing net names.

PCB review should cover:

  • Differential-pair membership and polarity.
  • Impedance, reference planes, layer transitions, and return paths.
  • Skew, pair spacing, via stubs, pads, and test-point discontinuities.
  • Connector placement and cable-bend clearance.
  • Customer-approved VBUS protection, grounding, shielding, and ESD parts.

EBest Circuit (Best Technology) can review the released PCB data for manufacturability and coordinate fabrication, component sourcing, PCBA, inspection, and agreed testing inputs. The customer remains responsible for USB topology, controller selection, electrical targets, firmware, compliance, and final system validation.

USB motherboard pinout
PCB layout review helps confirm differential-pair routing and connector integration.

USB Type C Header Integration Risks

For a front-panel Type-C header, control the connector revision, footprint, lane assignment, orientation handling, sideband signals, power architecture, and mating cable in one interface definition.

Before releasing a PCB, the engineering team should confirm:

  • Exact header and mating-cable part numbers and revisions.
  • Required data and power functions.
  • Lane, polarity, control, shield, and ground mapping across all files.
  • Clearance for the plug, cable exit, enclosure, and nearby hardware.

Do not freeze the footprint while the interface is changing. Confirming the connector first is cheaper than board rework or a replacement cable.

Motherboard USB Header PCB Checks

A correct schematic can still fail if the footprint is mirrored, library pins disagree, the connector hits the enclosure, or high-speed pairs cross a plane split. Review logical pin assignment and physical implementation together.

Key checks include:

  • Library verification: compare the schematic symbol, footprint, 3D model, and manufacturer drawing pin by pin.
  • Orientation control: show pin 1, key position, connector opening, cable exit, and inspection view on the assembly drawing.
  • Routing continuity: keep each differential pair together and review layer changes, return vias, stubs, and plane transitions.
  • Power protection: confirm the customer-approved fuse or switch, current limit, ESD network, decoupling, and grounding implementation.
  • Manufacturing clearance: verify annular ring or pad geometry, solder-mask dam, paste opening where applicable, courtyard, edge clearance, and rework access.
  • Test definition: identify accessible checks for continuity, shorts, power rails, connector orientation, and any approved functional fixture.

Release only a matched file set. A corrected assembly PDF cannot compensate for an old Gerber, centroid file, or BOM.

A USB Header PCBA Project Example

A representative USB header PCBA project involved an industrial controller board with conflicting connector, cable, and PCB release files.

Project background

An industrial-equipment team was preparing a pilot controller board. A keyed 2 x 5 USB 2.0 header served an internal touch display and a service port, but the BOM, connector drawing, cable drawing, footprint, and enclosure model came from different revisions.

What the pre-production review found

  • The schematic used a top view; the cable drawing showed the mating face without naming the view.
  • The generic BOM entry did not define the key position, height, or approved part number.
  • Pin 1 was marked on the PCB, but the mark would be partly hidden after the connector was installed, leaving assembly operators without a clear orientation reference.
  • The cable exit faced the enclosure wall, limiting insertion and bend clearance.

Actions and outcome

  • Purchasing waited for one controlled drawing that aligned pin numbers, mating view, wire map, and part number.
  • The keepout and nearby placement were adjusted for installation and cable bend.
  • Inspection added orientation and continuity checks; functional testing added enumeration on both ports.

After the files were aligned, the pilot build used one approved connector and one cable orientation. The review prevented reversed installation, enclosure rework, and USB enumeration failures during validation.

USB motherboard pinout
Connector orientation, cable drawings, and continuity checks should agree before production.

Files to Confirm Before PCB Fabrication and Assembly

A revision-controlled RFQ package reduces clarification and ensures suppliers quote the same USB interface.

Provide these inputs when applicable:

  • Fabrication data, drills, stackup, impedance requirements, and fabrication drawing.
  • Centroid data, assembly drawing, orientation notes, and panel requirements.
  • BOM with approved part numbers, alternates, and the exact USB header.
  • Schematic and controlled interface drawing.
  • Mating-cable drawing and enclosure/3D data when fit is critical.
  • Customer-approved inspection, functional test, fixture, firmware, and acceptance requirements.

Before production, withdraw obsolete files and confirm one revision across the release package. Update the full set when the connector or pin map changes.

FAQs About USB Motherboard Pinout

Is every 9-pin USB 2.0 motherboard header wired the same?

No. Many boards follow a common dual-port arrangement, but OEM or custom boards may use different keying or assignments. Verify the exact motherboard manual, board revision, connector drawing, and mating cable.

Can wire color confirm a USB motherboard pinout?

Wire color is only a clue. Confirm continuity and the released pin map because custom harnesses may not use the familiar red, white, green, and black convention.

Why does a USB 3.x motherboard header have more pins?

It commonly carries USB 2.0 compatibility signals plus dedicated SuperSpeed transmit and receive pairs, power, ground, and shielding or drain connections.

Can a USB 3.x header be adapted to a USB 2.0 front-panel cable?

An adapter may provide mechanical and signal conversion for a defined application, but it does not guarantee speed, power, controller support, or correct wiring. Check both specifications and the adapter pin map.

What should a PCB supplier receive to verify a USB header build?

Provide the controlled fabrication and assembly package, BOM, connector part number, schematic or interface drawing, mating-cable information, and customer-approved inspection and test requirements.

Need a pre-production review or quotation for a PCB or PCBA with a USB motherboard pinout? Email your fabrication data, BOM, connector and cable drawings, and test requirements to sales@bestpcbs.com. EBest Circuit can review the package before fabrication and assembly.

You may also like