PCB manufacturing PCB manufacturing
Home > Blog

Kelvin connection

Four Terminal Sensing PCB Layout for Accurate Measurements
Saturday, September 26th, 2026

Four terminal sensing helps reduce low-resistance measurement errors caused by resistance outside the component being measured. Copper traces, pads, contacts, and solder joints may each contribute only a small amount, but those added resistances become significant when the target value is measured in milliohms.

Four terminal sensing reduces this error by separating the current-carrying path from the voltage-sensing path. Achieving that benefit on a finished PCBA requires more than adding two sense traces to a schematic: the connection points, pad geometry, current flow, copper routing, solder distribution, and component placement must all preserve the intended Kelvin connection. EBest Circuit manufactures and assembles customer-designed PCBs and PCBAs with Kelvin connections, helping customers reduce avoidable measurement errors and maintain better consistency from prototypes to repeat production.
four terminal sensing
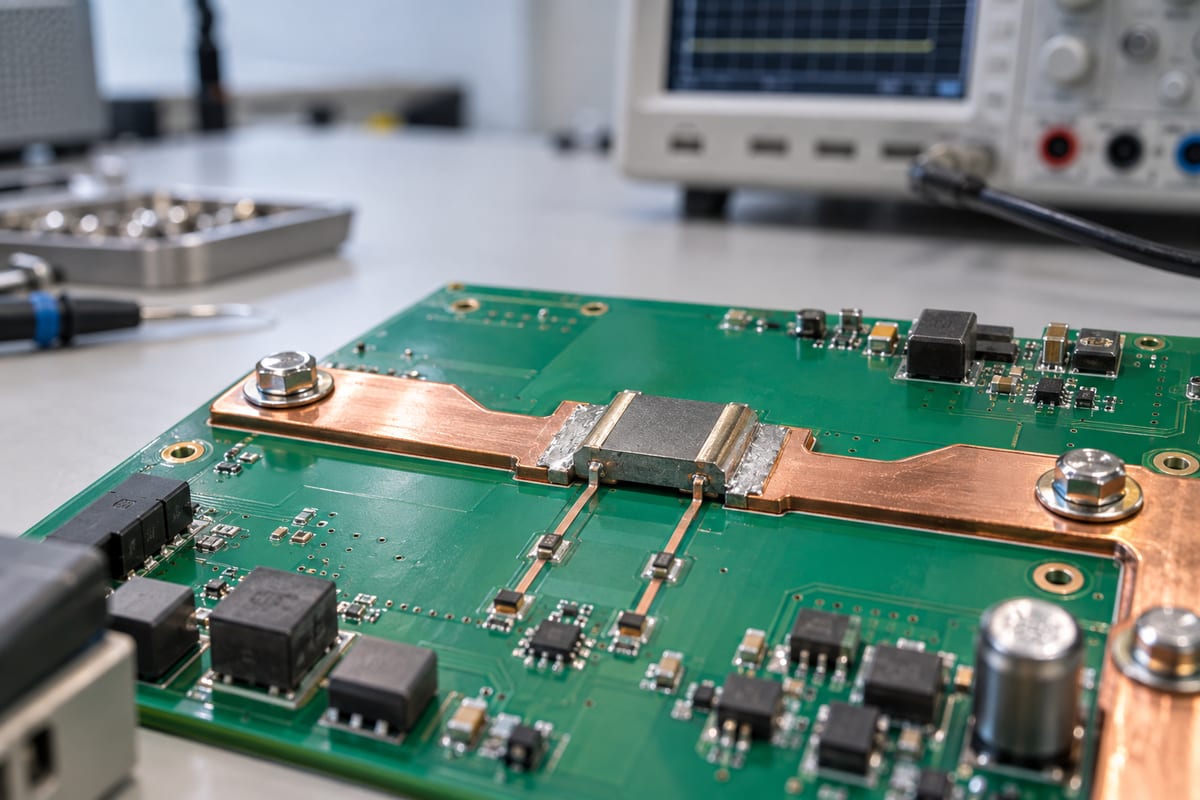
A Kelvin-connected shunt uses separate current and voltage-sensing paths on the PCB.

What Is Four Terminal Sensing and Why Does It Improve Low-Resistance Measurements?

Four terminal sensing, also called four-wire sensing or Kelvin sensing, separates the current-carrying connections from the voltage-measuring connections. This allows the circuit to measure the resistance element without including most of the unwanted voltage drop in the conductors and connection points.

  • Force path: Two connections carry current through the resistor. Their traces, pads, and solder joints may create additional voltage drop, especially at high current.
  • Sense path: Two separate connections measure voltage at the designated points on the resistor. Because the sense inputs draw very little current, voltage drop along these traces is extremely small.

This separation is especially valuable when measuring a current shunt, power connection, busbar interface, battery path, or another milliohm-level resistance. It does not eliminate errors from component tolerance, temperature coefficient, amplifier offset, noise, thermal gradients, or calibration; it specifically reduces the error introduced by shared conductors and connection resistance.

How Does Four Terminal Sensing Differ from Two-Wire Resistance Measurement?

The practical difference is whether the same conductors or separate conductors carry current and measure voltage.

  • Two-wire resistance measurement: The same path carries current and measures voltage. The result can include voltage drops from PCB traces, pads, solder joints, connectors, cables, and test leads.
  • Four terminal sensing: The force connections carry current, while separate sense connections measure voltage close to the resistance element. Most of the voltage drop in the high-current conductors is therefore excluded from the measurement.

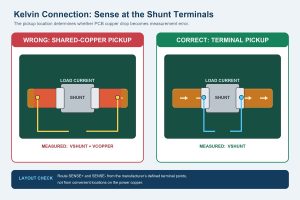
For a milliohm-level shunt, even a short shared copper section can shift the reading. Moving the sense connection from the load trace to the designated point on the resistor pad can exclude that shared copper. Two-wire measurement may be sufficient when conductor resistance is insignificant, but four terminal sensing becomes more valuable as resistance decreases, current increases, or allowable error becomes tighter.

How Should a Kelvin Connection Separate Force and Sense Current Paths?

A Kelvin connection should keep the force and sense paths electrically separate until they reach the intended measurement points. If they share copper before reaching the resistor, the voltage drop across that shared section becomes part of the measurement.

  • Route the force path through the load-current regions. Wider force copper should enter and leave through the parts of the pads intended to carry current and control temperature rise.
  • Connect the sense traces directly to the sensing points. They should not branch from a force trace farther away from the resistor.
  • Keep the two sense traces short and reasonably balanced. They should avoid switching nodes and high-current loops that may couple noise into a small differential signal.
  • Place vias without creating shared load-current copper. A via may help escape a dense area, but the sense signal should not pass through copper that also carries the load current.
four terminal sensing
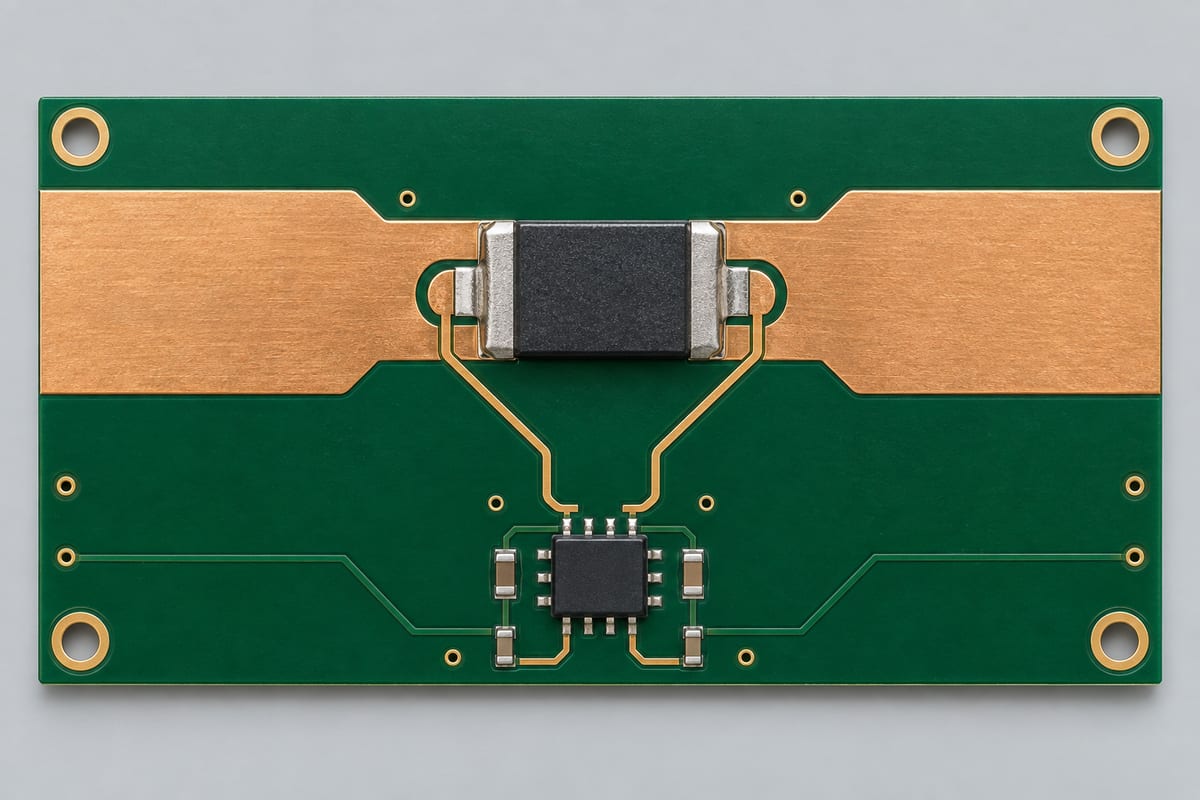
Wide force-current copper and dedicated sense traces meet the shunt at separate connection points.

The approved PCB data should make this physical separation unambiguous so that fabrication and assembly reproduce the intended connection rather than interpret it.

Where Should Sense Traces Meet the Shunt Resistor Pads?

Sense traces should meet the shunt resistor at dedicated points that exclude unwanted voltage drop from the load-current copper and solder connections. The exact location depends on the resistor package and its approved footprint.

  • For a two-terminal shunt: Each sense trace commonly approaches the inner portion of a split pad, while load current enters through a different part of the copper. This reduces the pad and trace resistance shared by the force and sense paths.
  • For a four-terminal resistor: Each sense trace connects to its dedicated sense terminal. The PCB must keep that terminal separate from the force copper until the intended measurement point; reconnecting it too early can reintroduce unwanted voltage drop.

Current distribution around the pads also matters. If load current enters one side of a shunt unevenly, the voltage across the pad surface will not be uniform. Symmetrical copper entry and clearly defined sensing locations reduce the risk of a repeatable offset caused by pad resistance or solder distribution. The approved land pattern should therefore leave no uncertainty about where the measurement begins.

How Does PCB Layout Affect Four Terminal Sensing Accuracy?

PCB layout determines which voltage drops the sense circuit includes and which ones it excludes. A correct schematic can therefore produce an inaccurate assembled board if the physical current path is not controlled.

  • Shared copper: Any section used by both force and sense paths can add a load-dependent voltage drop to the measurement.
  • Sense-point location: Moving a sense connection along a pad or trace changes how much pad and copper resistance is included in the measured voltage.
  • Current distribution: Pad shape, neck-down regions, copper pours, thermal reliefs, and nearby vias influence how current enters the resistor. Uneven entry can create unequal voltage distribution around the terminals.
  • Noise coupling: Sense traces routed near switching nodes, inductors, gate-drive loops, or fast current transients can pick up noise that obscures a small differential signal.
  • Thermal conditions: Heat from the shunt, power devices, or unequal copper areas can affect the resistor and nearby measurement circuitry.

The best layout is not simply the one with the shortest traces. It is the one that controls what the sense circuit measures, maintains predictable current flow, limits noise coupling, and can be reproduced consistently in fabrication and assembly.

When Should a PCB Use a Four-Terminal Resistor or a Split-Pad Footprint?

  • Use a dedicated four-terminal resistor when measurement accuracy and repeatability are critical and a suitable component is available in the required resistance, power, tolerance, temperature coefficient, and package size. Its separate terminals establish a physical distinction between force and sense connections.
  • Use a split-pad footprint around a two-terminal shunt when the approved BOM already specifies that component, sourcing options are limited, board space is constrained, or the customer has validated the footprint in the operating circuit.

These approaches are not automatically interchangeable. A four-terminal component reduces dependence on custom pad segmentation and makes the connection intent easier to reproduce. A split-pad footprint offers compatibility with an existing two-terminal shunt but depends more heavily on the pad geometry and current-entry pattern.

The choice should be based on electrical accuracy, power dissipation, thermal behavior, package availability, cost, board space, and validation results. After the component and footprint have been approved, their measurement-critical geometry should not be changed during DFM or production without customer review. A seemingly minor adjustment to pad divisions, copper entry, or sense-point location can change what the circuit measures.

How Can PCB Fabrication and Assembly Preserve Kelvin Sensing Accuracy?

PCB fabrication and assembly preserve Kelvin sensing accuracy by reproducing the approved force and sense geometry without introducing variations that change current flow or connection resistance.

  • During fabrication: The split-pad spacing, copper entry, sense-trace connection points, vias, and solder-mask boundaries must remain consistent with the approved data. Unauthorized copper smoothing or pad modification near the shunt can alter the electrical boundary even when the board remains fully connected.
  • During assembly: Solder-paste distribution and component placement are especially important around divided or asymmetric pads. Excessive placement offset or uneven solder volume can change how the terminals contact the pads and how current enters the resistor. The assembly process should also avoid solder bridging across regions intended to remain electrically distinct.
  • AOI: Confirms component position, orientation where applicable, and visible solder conditions.
  • X-ray: Helps examine relevant joints or structures that are hidden from optical inspection.
  • Electrical testing: Verifies measurement performance when the customer defines the limits, current conditions, fixtures, and procedures for the intended application.

AOI and X-ray can verify assembly quality, but they do not by themselves prove sensing accuracy. Electrical testing is required when the finished PCBA must be evaluated against a defined measurement limit.
four terminal sensing
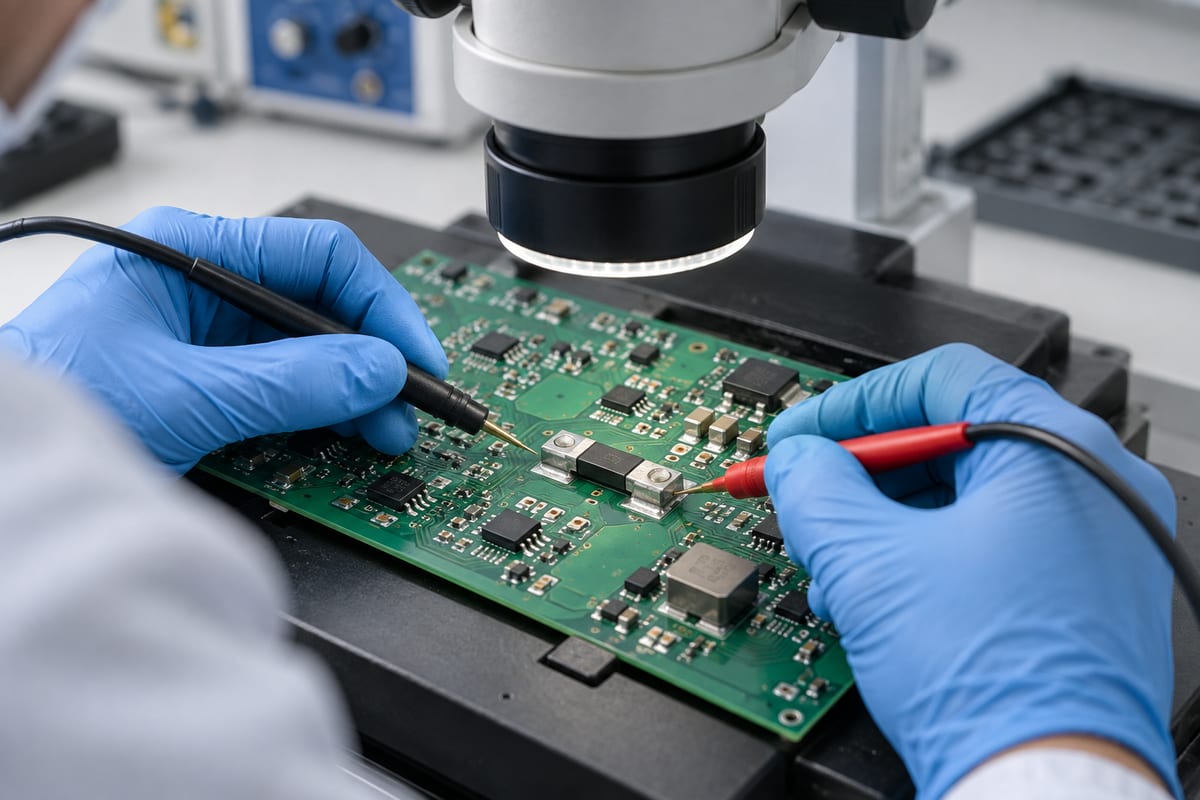
Inspection and customer-defined electrical testing help verify assembly quality and measurement performance.

When critical pad geometry, solder volume, and component placement remain consistent, a validated prototype is more likely to move into repeat production without unexpected measurement shifts between batches.

FAQs About Four Terminal Sensing

Is four terminal sensing the same as Kelvin sensing? In most PCB current-measurement applications, yes. Both terms describe the use of separate force and sense connections so that conductor and contact resistance in the force path has less influence on the measured voltage.

Does four terminal sensing require a four-terminal resistor? No. A dedicated four-terminal resistor provides separate physical terminals, but a validated split-pad footprint can create Kelvin connections around a two-terminal shunt. The component and footprint must be evaluated together.

Can four terminal sensing eliminate all current-measurement errors? No. It primarily reduces errors caused by shared conductor and connection resistance. Resistor tolerance, temperature coefficient, amplifier errors, noise, thermal effects, and calibration can still affect the complete measurement.

Why can boards made from the same schematic produce different readings? The schematic does not define every physical detail of current flow. Differences in sensing-point location, pad geometry, copper distribution, solder volume, component placement, and temperature can change the measured voltage even when the electrical connections appear identical.

Should Kelvin sense traces be routed as a differential pair? They should generally be kept close, balanced, and away from noise sources, but the required geometry depends on bandwidth, amplifier architecture, signal level, and the customer’s circuit. They should not automatically be treated as a controlled-impedance high-speed differential pair.

Can a PCB manufacturer change the Kelvin footprint during DFM? A manufacturer may identify a manufacturability concern and recommend a change, but it should not silently alter measurement-critical geometry. Changes to sense-point locations, split pads, copper entry, or terminal assignments require customer review and approval.

EBest Circuit manufactures and assembles customer-designed PCBs and PCBAs with Kelvin connections, from prototypes through repeat production. We focus on preserving the approved force and sense separation through PCB fabrication, component placement, soldering, inspection, and agreed testing so the finished board can deliver more consistent low-resistance measurements. If you are preparing a four terminal sensing PCB or PCBA, send your Gerber files, BOM, assembly data, quantities, and testing requirements to sales@bestpcbs.com for a manufacturability review and quotation.
You may also like

Shunt Resistor Selection and PCB Layout for Accurate Sensing
Tuesday, August 18th, 2026

A shunt resistor circuit can be correct on the schematic and still produce inconsistent readings on assembled boards. At milliohm resistance levels, the PCB copper, pad entry, solder joints, temperature, and measurement nodes can contribute error that the basic calculation never shows.

The safest approach is to treat the shunt resistor, PCB layout, BOM, and acceptance test as one measurement system. This guide shows what to calculate, what to inspect in the layout, what to lock before purchasing, and what evidence to request from the PCBA build.

shunt resistor

What Is a Shunt Resistor?

A shunt resistor, also called a current sense resistor, is a low-value resistor placed in the load-current path. Using a shunt resistor for measuring current is straightforward in principle: current creates a proportional voltage across the part. The voltage across it is proportional to current: V = I × R. A current-sense amplifier or ADC reads that voltage and converts it into a measurement or protection decision.

At 1 mΩ, every ampere produces only 1 mV. That makes the physical sense points important: copper, pads, solder joints, and amplifier offset can become a meaningful share of the signal. A precise component does not guarantee a precise assembled measurement.

Define three groups of requirements before selecting the part:

  • Electrical range — minimum, normal, maximum, surge, and fault current.
  • System limits — permitted voltage drop, power loss, response time, and accuracy over temperature.
  • Architecture — high-side or low-side sensing and a two-terminal or four-terminal shunt.

How Does Shunt Resistor Current Measurement Work?

A 2 mΩ shunt carrying 30 A gives three immediate results:

  • 60 mV across the shunt — confirm that the load can tolerate this voltage loss.
  • 1.8 W in the resistor — verify the derated thermal capacity in the real enclosure.
  • 2.4 V after a gain of 40 — confirm amplifier and ADC headroom, including faults and tolerances.

Accuracy must then be checked as a chain. Resistor tolerance sets the starting error. Temperature coefficient changes the resistance as the part heats. Amplifier offset becomes significant when the sense voltage is small. Gain error, ADC reference error, noise, and any copper included between the real sense points add further uncertainty.

Do not specify accuracy only at room temperature and nominal current. Define at least a low-current point, a normal operating point, and a high-current point after thermal stabilization. If the circuit also protects against faults, add the trip current, response time, and allowed recovery behavior. These become the basis of calibration and production testing.

Use the symptom to narrow the cause. A large percentage error at low current usually points first to offset, noise, or incorrect sense points. Drift that appears only after high-current warm-up points more strongly to shunt TCR, temperature rise, or heated copper. A consistent gain error across the range may be calibratable; unstable board-to-board variation usually requires a material, layout, assembly, or fixture investigation.

shunt resistor

How Do You Select a Shunt Resistor?

Calculate a provisional resistance from the maximum sense voltage divided by maximum current. A shunt resistor calculator can speed up the resistance and power calculation, but it cannot validate thermal margin, pulse capability, PCB copper, or sense-point placement. Then calculate continuous power with P = I²R and pulse energy for overload events. Apply the component manufacturer’s derating curve rather than assuming the printed wattage is available under every PCB and airflow condition.

Next compare tolerance, TCR, pulse rating, terminal design, package, land pattern, operating temperature, and supply status. For example, a low TCR helps control drift, but it does not compensate for a hot copper neck-down beside the resistor or a sense trace connected outside the intended terminal point.

Lock these purchasing decisions in the RFQ and BOM:

  • State the exact manufacturer part number and whether substitutions are prohibited or require approval.
  • For any alternate, require matching resistance, tolerance, TCR, continuous and pulse ratings, terminal structure, package, and recommended footprint.
  • Name the person who must approve an alternate before components are purchased or loaded onto the SMT line.

This prevents a common failure: accepting a resistor because its nominal value and package appear correct, while its thermal behavior, pulse capability, or terminal geometry changes the actual measurement and assembly result.

Shunt Resistor vs Hall Effect Sensor

Choose a shunt when the product can tolerate a small voltage drop and needs a compact, fast, cost-effective measurement. Consider a Hall effect sensor when galvanic isolation or lower conductive loss is more important. Neither option is automatically more accurate; each moves the dominant errors to different parts of the system.

DecisionShunt resistorHall effect sensor
IsolationNo inherent galvanic isolationIsolated options available
Power lossI²R loss in the load pathLow conductive insertion loss
Key error sourcesTCR, offset, copper, sense-point locationOffset, magnetic noise, external fields
PCB prioritiesCurrent path, Kelvin routing, heatFootprint, supply, magnetic clearance
Best fitDirect, compact measurement where loss is acceptableIsolation or low conductive loss is required

For procurement, compare the complete implementation rather than component price alone. A shunt solution needs controlled copper, Kelvin sensing, heat management, and a suitable amplifier. A Hall solution may need more board area, supply routing, magnetic clearance, and calibration. The approved architecture should reflect isolation, bandwidth, accuracy, fault response, space, and lifecycle requirements.

Kelvin Connection for a Shunt Resistor

A Kelvin connection separates the voltage-sense path from the high-current path. The two sense traces begin at defined points on the resistor terminals, so voltage drop in the surrounding power copper, vias, pads, and high-current solder path is excluded from the measurement.

Review the layout in this order:

  • Avoid a narrow or asymmetric current entry. Prefer a short, balanced path into both shunt terminals, without unreviewed neck-downs or thermal reliefs.
  • Avoid taking SENSE+ and SENSE- from convenient points on a copper pour. Prefer connections at the terminal locations recommended by the shunt manufacturer.
  • Avoid separating the two sense traces or routing them beside switching nodes. Prefer a close, balanced pair kept away from gate-drive loops and inductors.
  • Avoid sharing sense or reference copper with load-current return. Prefer dedicated low-current paths from the shunt to the amplifier.

For a four-terminal shunt, keep current pads and sense pads distinct. For a two-terminal shunt, pad geometry and trace entry become even more important. A schematic net name does not prove that the physical connection is correct; the copper must be reviewed at the resistor terminals.

Place any approved input filter symmetrically and close to the amplifier. Keep test points on the same nodes used by the measurement circuit. If a fixture measures from different locations, it can pass a board that the product itself reads differently.

A Kelvin error often looks deceptively correct on one prototype. Calibration may remove the error at one current and temperature, but it cannot make changing copper drop disappear across load, temperature, and production variation. If the reading changes when the current path heats, inspect the physical sense-point location before changing calibration constants.

shunt resistor

What Can Distort Current Measurement After Assembly?

Assembly introduces variation that is absent from the schematic. Unequal solder volume can move the effective current-entry point. Poor wetting can increase local resistance. Mechanical stress and board flex can affect the resistor, while heat from nearby components can shift both the shunt and amplifier behavior.

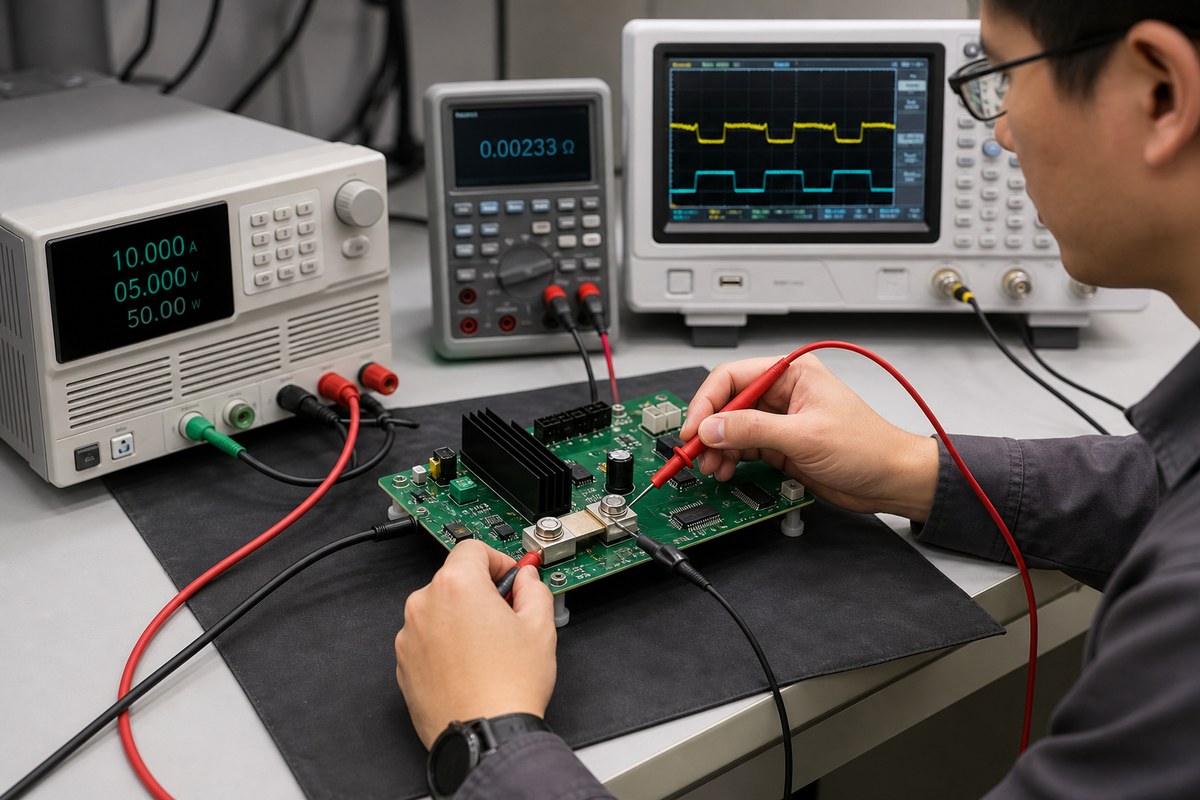
Visible inspection is necessary but not sufficient. AOI can verify component presence and visible solder condition; X-ray can help with hidden connections. Neither proves electrical accuracy. A useful test must specify current, measurement nodes, warm-up or dwell time, temperature condition, acceptance limits, and the result to record.

Use four controls with different purposes:

  • Incoming material — verify the approved manufacturer, part number, lot information, and any required traceability.
  • Assembly workmanship — inspect placement, solder wetting, bridging, contamination, damage, and component seating.
  • PCB implementation — confirm the released current path, Kelvin points, copper construction, and revision were actually built.
  • Electrical acceptance — apply customer-defined current points and verify the measured output, trip behavior, or calibration result within the approved limits.

Example production test plan

  • Test at 10%, 50%, and 100% of the approved operating current.
  • Use the same Kelvin nodes read by the product, not convenient fixture points elsewhere on the power copper.
  • At the high-current point, record the result after the defined warm-up or thermal-stabilization period.
  • Retain input current, shunt voltage, amplifier or ADC output, calculated error, and pass/fail result.

The exact current points and limits must come from the customer’s approved specification; the example shows the level of detail needed for a repeatable test.

Different symptoms suggest different checks: low-current instability calls for noise and offset review; high-current drift calls for thermal review; large board-to-board spread calls for BOM, solder, copper, and fixture comparison. This diagnostic order prevents repeated calibration from hiding a manufacturing problem.

A Shunt Resistor PCB Assembly Example

An ADC current-sensing PCBA project illustrates how an electrical requirement becomes a manufacturing package. The board used four-layer FR-4 with Tg150 material, 2 oz copper on the inner and outer layers, 1.6 mm thickness with ±10% tolerance, and lead-free HASL.

The customer first reviewed the production data and panelization files before fabrication. This created a clear release point: manufacturing preparation could proceed only after the customer confirmed that the production package still represented the intended board.

The SMT build also assigned clear responsibilities:

  • EBest sourced all components, keeping material responsibility with one assembly partner.
  • The boards were separated after SMT and delivered as individual units, so the required delivery format was defined before production.
  • Post-SMT cleaning required the boards to be free of solder balls and other contamination before shipment.

The customer value came from the sequence: define the board construction, approve the production interpretation, assign component responsibility, specify the delivery condition, and make cleanliness an acceptance requirement. Each control removed a different source of ambiguity before shipment.

For a similar project, add the electrical acceptance layer before quotation: the exact shunt part number, approved Kelvin nodes, operating and fault-current range, allowed error, test current points, warm-up condition, and required test record. That gives the manufacturer something objective to build and verify.

The project followed a practical handoff: the customer defined and approved the production interpretation; EBest controlled board construction, sourcing, SMT, separation, and cleanliness; electrical acceptance still required customer-approved current points and limits. That division gives both sides a clear decision before material purchase and a clear acceptance basis before shipment.

What Files Support a Shunt Resistor PCBA Review?

Send one revision-controlled package. At minimum, it should contain Gerber or ODB++ data, fabrication drawing, BOM, pick-and-place file, assembly drawing, and test specification. Mismatched revisions can invalidate an otherwise careful review.

Use each file to answer a specific production question:

  • Fabrication data — What stackup, copper weight, thickness, finish, current-path geometry, and critical dimensions must be built?
  • BOM — Which exact shunt, amplifier, filter components, and approved alternates may be purchased?
  • Assembly data — Where is each part placed, what workmanship or stencil notes apply, and which areas require special inspection?
  • Test specification — Which current is applied, where is voltage measured, how long must the board stabilize, what limits apply, and what evidence is retained?

Also state quantity, prototype or production stage, delivery format, traceability needs, and first-article requirements. For functional testing, provide the fixture interface, power sequence, firmware state, safe operating limits, calibration instructions, and pass/fail criteria.

EBest Circuit can review the manufacturing package, fabricate the PCB, support controlled component sourcing, assemble and inspect the board, and coordinate agreed testing. Circuit architecture, the accuracy budget, safety requirements, and final product validation remain customer-controlled decisions.

Shunt Resistor FAQs

What resistance value should a shunt resistor use?

Start with maximum current and permitted sense voltage, then verify continuous power, transient energy, temperature rise, amplifier range, and the full error budget. There is no universal best resistance value.

Why is a Kelvin connection important for a shunt resistor?

It prevents voltage drop in shared high-current copper and pad paths from being included in the sensed voltage. The smaller the shunt value and signal, the more important the physical sense-point location becomes.

Can a normal resistor replace a current-sense resistor?

Not without review. In a shunt resistor vs normal resistor comparison, nominal resistance alone is not enough. Tolerance, TCR, continuous and pulse ratings, terminal structure, package, land pattern, and thermal behavior must meet the approved requirements.

Can AOI verify shunt resistor accuracy?

No. AOI can verify visible assembly conditions and component presence. Accuracy requires an electrical test with defined current, nodes, temperature or warm-up condition, limits, and records.

What should be sent for a shunt resistor PCBA quotation?

Send controlled PCB data, fabrication drawing, BOM, pick-and-place file, assembly drawing, and test requirements. Include the current range, critical sense points, approved parts, quantity, delivery format, and required records.

Need a Shunt Resistor PCBA Review? Send your PCB data, fabrication drawing, BOM, assembly files, current range, and test requirements to sales@bestpcbs.com. EBest Circuit can review the manufacturing package and help align PCB fabrication, component sourcing, assembly, inspection, and agreed testing before quotation.

You may also like