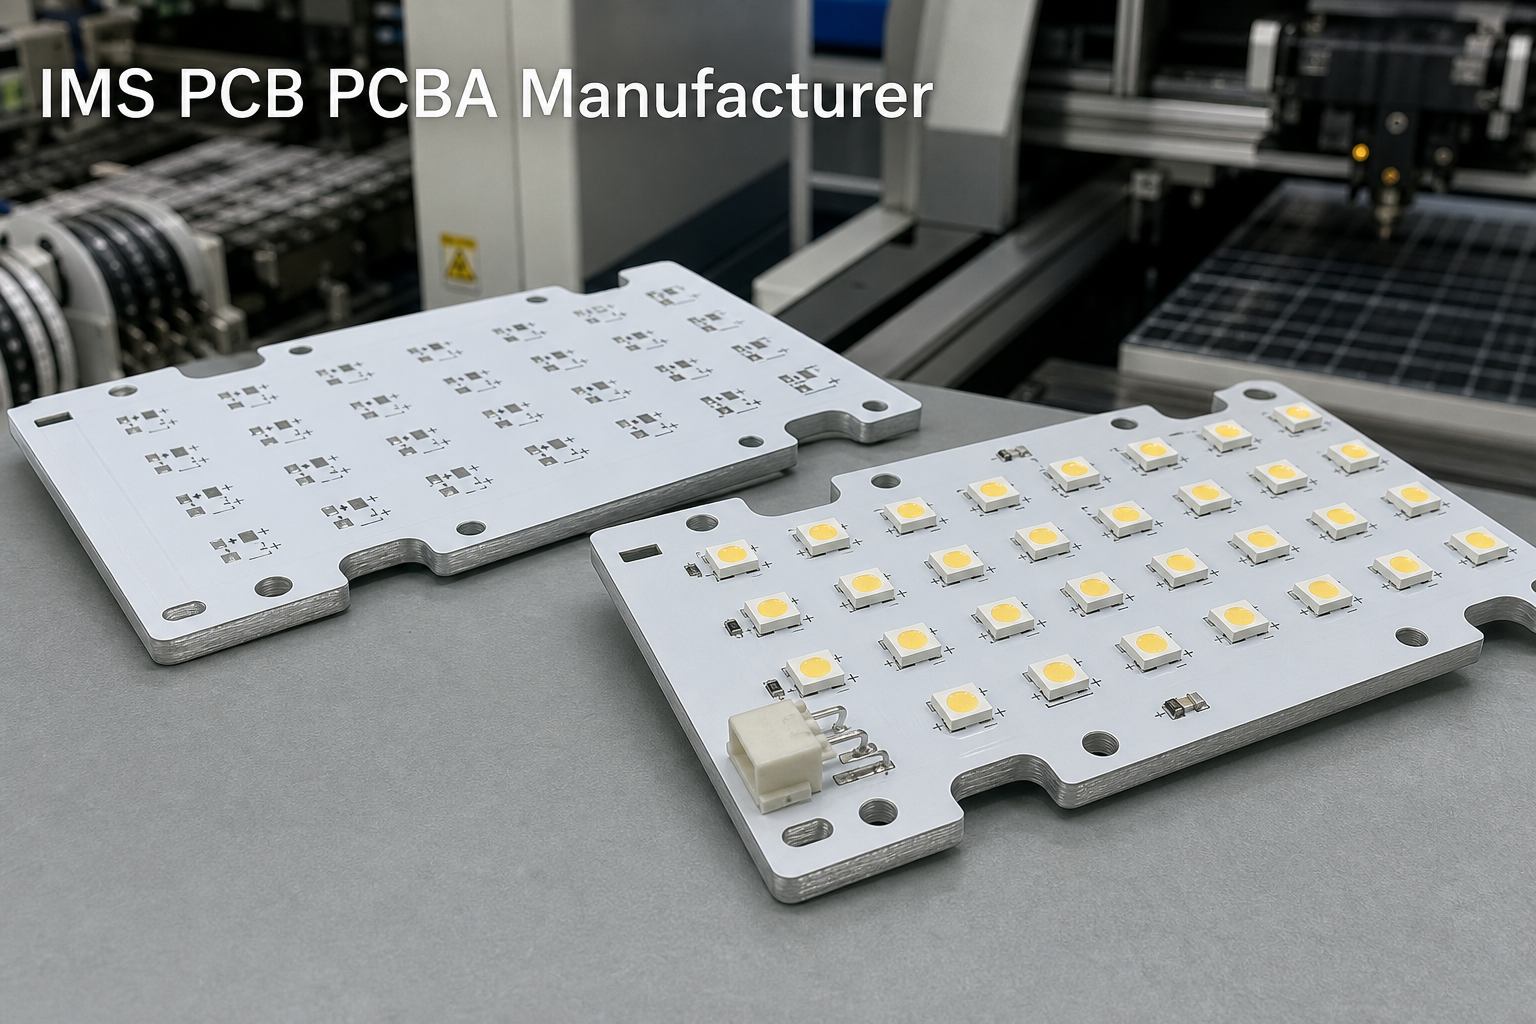
An IMS PCB PCBA manufacturer can help you turn your board design into an assembled product with fewer supplier handoffs. For insulated metal substrate (IMS) boards, reviewing fabrication, components, and assembly together helps catch mismatches before they interrupt production.
EBest Circuit (Best Technology) combines metal-core PCB manufacturing, component sourcing, and SMT assembly, so you can order bare boards or bring these stages together with one supplier. Email your available files and project requirements to sales@bestpcbs.com. We can review what you have and help identify the next steps toward a quote.
Bare IMS boards and assembled LED boards in one manufacturing workflow. AI-generated illustration.
What Can You Order from an IMS PCB PCBA Manufacturer?
You can keep your existing assembly arrangement or have EBest handle fabrication and assembly together. The right choice depends on the work you want to keep in-house and what you need delivered.
Choose the supply arrangement that fits your project:
Service
Includes
Best fit
Bare IMS PCB
Board fabrication
Existing assembly partner
PCB + components
Bare boards and purchased parts
Coordinated material supply
PCB + SMT assembly
Fabrication and assembly
Customer-supplied or mixed parts
Turnkey IMS PCBA
PCB, parts, and assembly
One manufacturing supplier
Optional services
Testing, cleaning, or wiring
Additional delivery requirements
Clear pricing makes these options easier to compare. During quotation review, we can clarify which components, tooling, tests, depaneling, and packaging are included, helping you budget for the finished order rather than just the bare board.
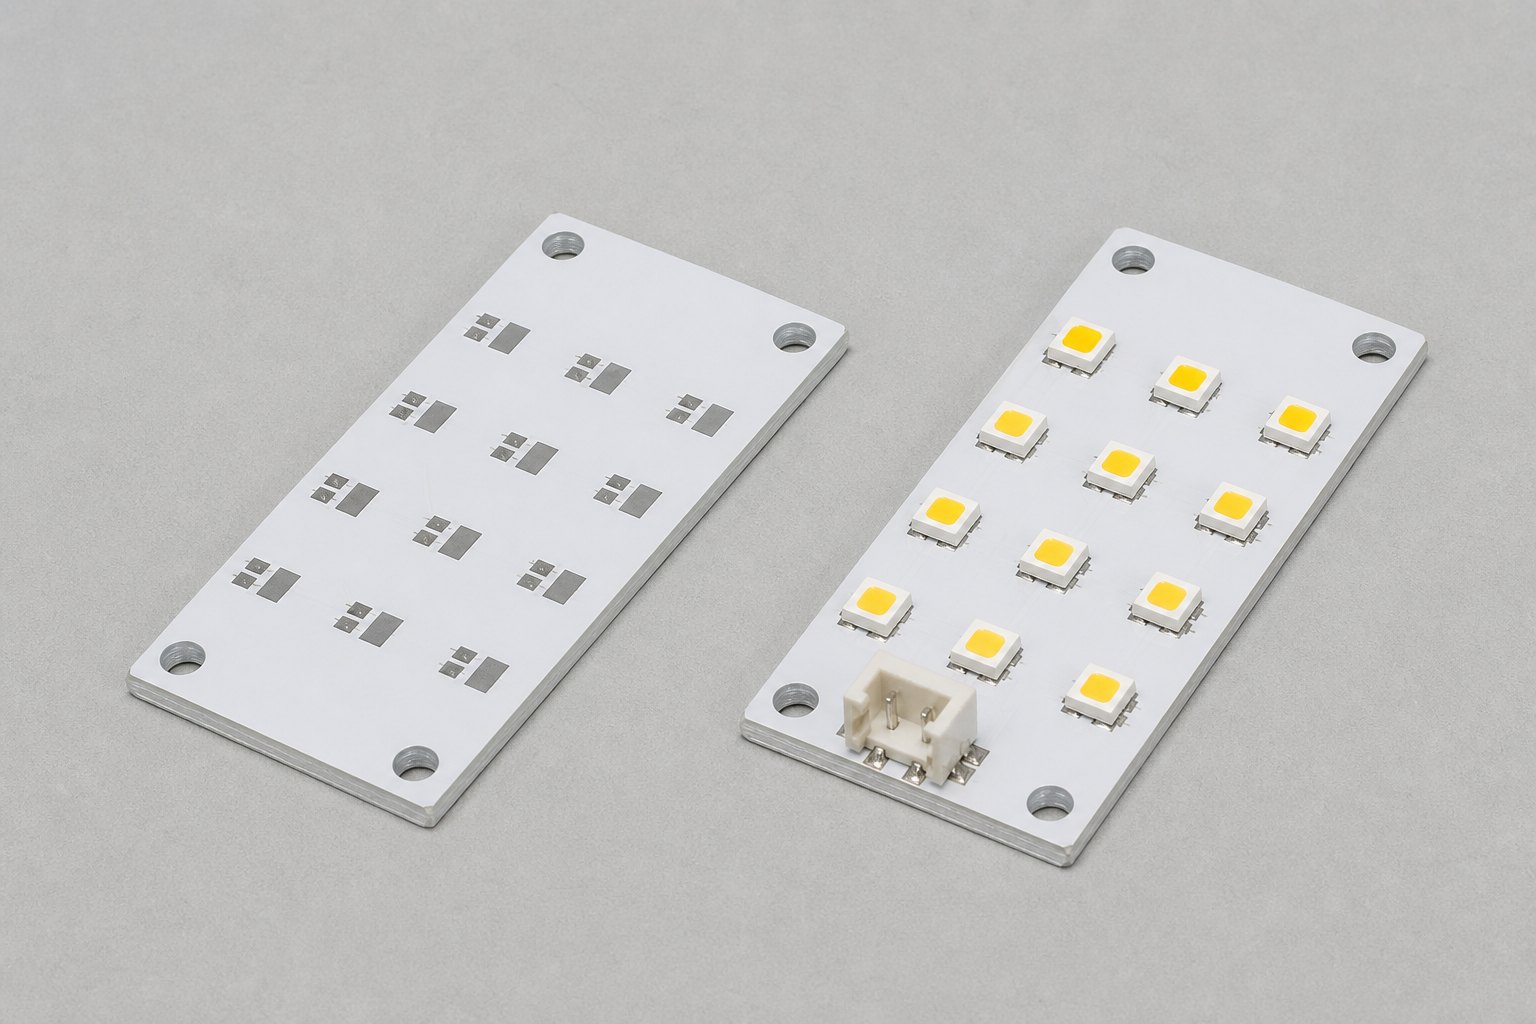
Bare and assembled aluminum-core boards illustrate two supply options. AI-generated illustration.
Can Your IMS PCB Material Meet Your Assembly Requirements?
Reviewing the material and assembly requirements together can help you avoid buying boards that need changes before they can be assembled. The key is to check the board construction, surface finish, and component requirements before fabrication starts.
An IMS board combines a metal base, a thermally conductive insulating layer, and circuit copper. Two boards described as “aluminum PCB” may still have different insulation layers, copper weights, and thicknesses. Reviewing these details against your design helps establish whether the proposed board meets your manufacturing requirements.
An early review helps address five common sources of rework:
Material mismatches. Checking the metal base, insulation layer, copper weight, and thickness against your design helps prevent an unsuitable substitution.
Soldering conflicts. Reviewing board and component temperature limits together helps identify restrictions on the assembly process.
Finish and storage issues. Confirming the surface finish and handling requirements helps plan how boards will be stored before soldering.
Installation problems. Mounting holes, connector access, component height, and heat-sink clearances need to match the intended assembly.
Panel changes. A panel suitable for fabrication may need adjustments for component placement or separation after assembly.
If a material detail is still open, share the drawing or existing specification. EBest can flag questions for your engineering team before purchasing begins. This manufacturing review supports your design; final thermal performance still needs validation in the finished product.
Why Choose EBest Circuit as Your IMS PCB PCBA Manufacturer?
With EBest, you can discuss the bare board, purchased parts, and assembly in one place. That means less work transferring requirements between suppliers and a clearer view of what your order includes.
Here is how that helps your project:
Less coordination between suppliers. Fabrication and assembly questions can be reviewed together, reducing the information you need to relay between separate companies.
Flexibility over component supply. You can discuss full sourcing or retain control of selected parts through a mixed-supply arrangement.
Fewer gaps between fabrication and assembly. Board construction, panel layout, component placement, and delivery format can be reviewed within the same order.
Whether your priority is fitting an existing housing, keeping specified components, or meeting a prototype deadline, sharing that priority early helps focus the review on what matters to your project.
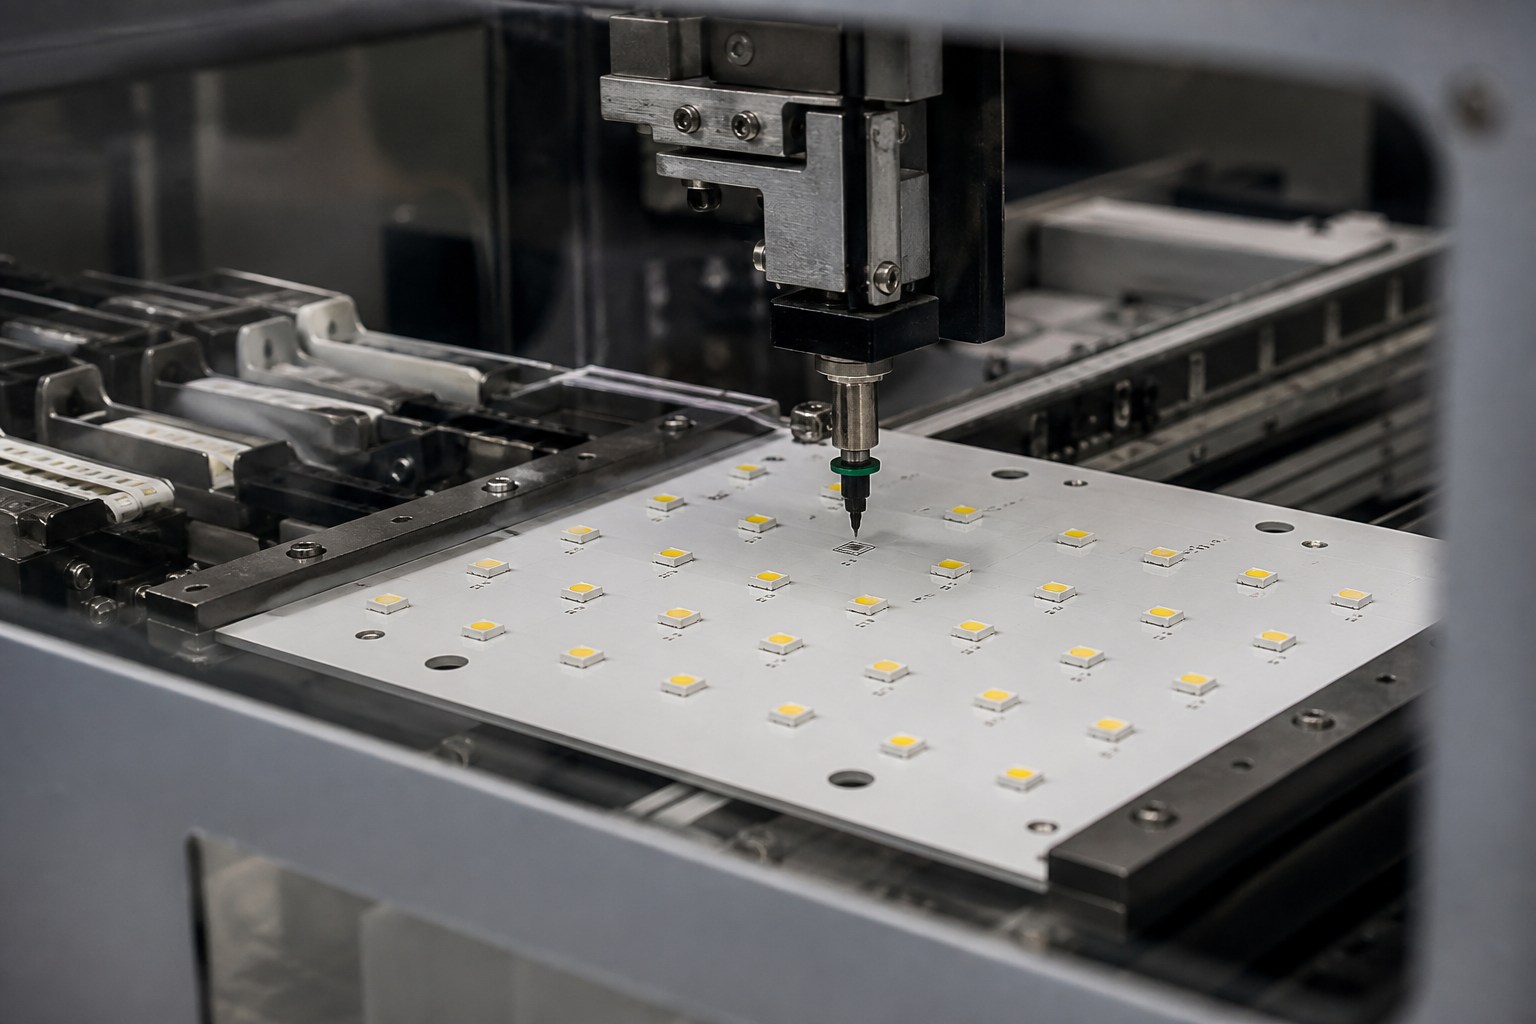
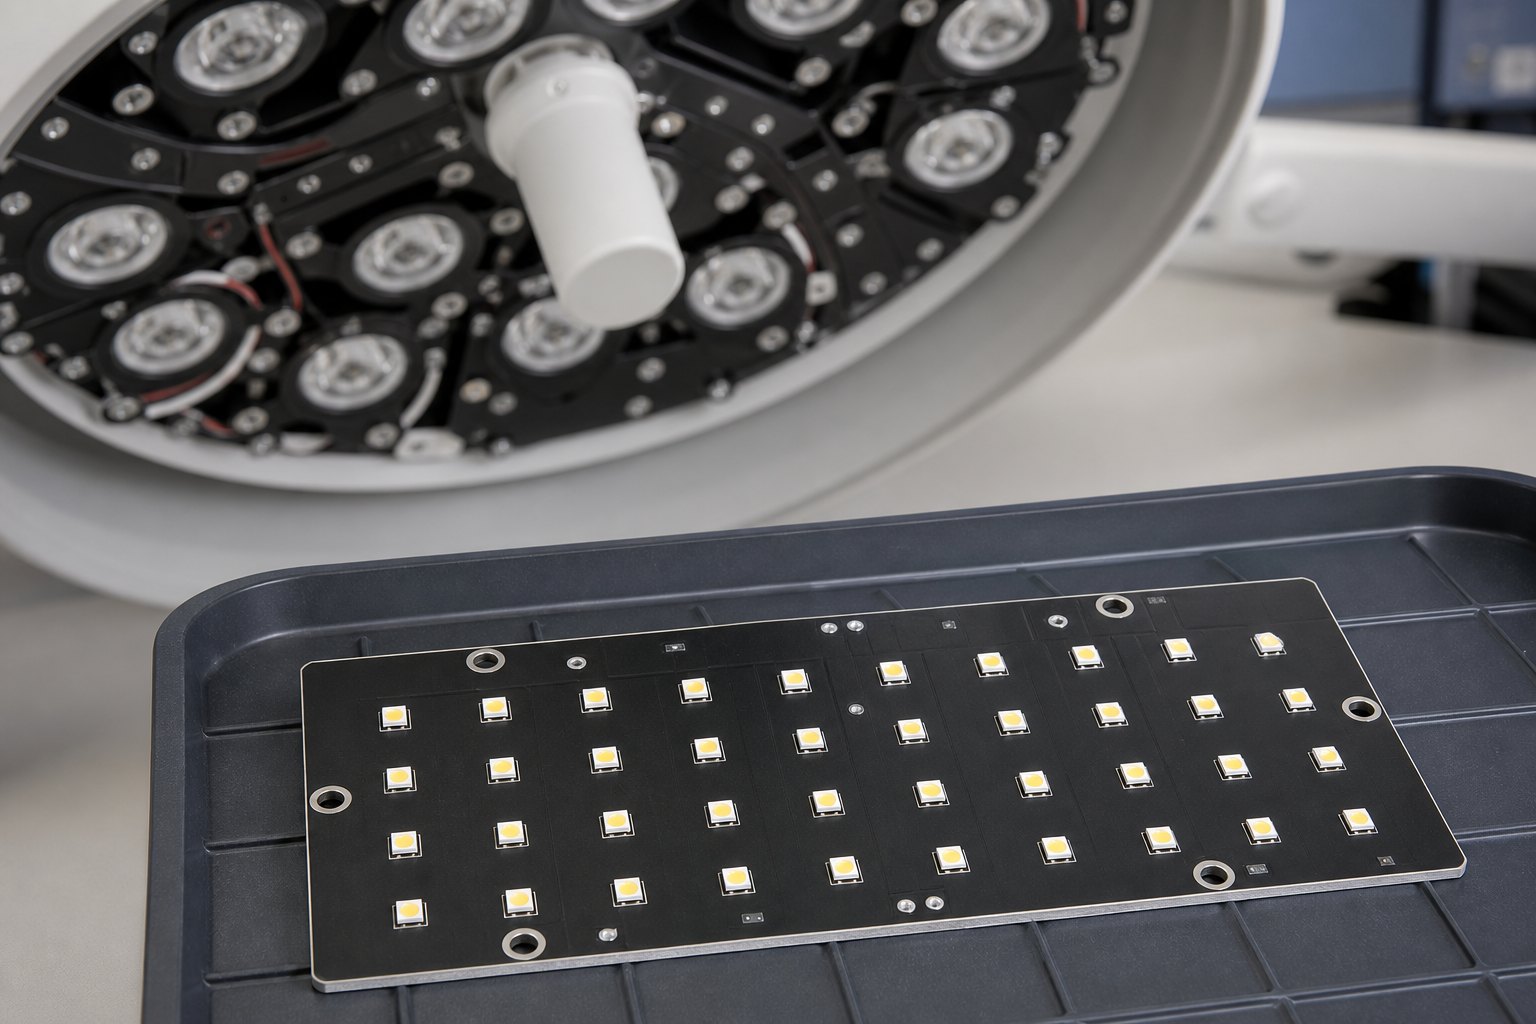
Illustrative SMT placement of LED components on an aluminum-core PCB. AI-generated illustration.
How Soon Can You Receive Your Assembled Boards?
If you have a prototype deadline, EBest can review normal and expedited production options against your target date. Standard single-layer aluminum MCPCB prototypes have a reference fabrication time of 4 days, or 24 hours for eligible expedited orders. PCBA has a separate reference of 1 week, with an expedited option of 2 days.
Use these production times for initial planning:
Stage
Normal
Fastest
1-layer MCPCB
4 days
24 hours
2-layer MCPCB
14 days
168 hours
4-layer MCPCB
21 days
To confirm
PCBA
1 week
2 days
The MCPCB references apply to prototype orders totaling less than 1 m², using standard aluminum material, 0.8–2.0 mm thickness, the listed standard copper options (H/H or 2 oz), lead-free HASL, white solder mask, black silkscreen, and 0.8 W/(m·K) thermal conductivity. Different materials, constructions, or finishes require a project-specific schedule.
For your assembled order, EBest can confirm a schedule covering fabrication, component sourcing, assembly, and inspection. A 24-hour board service and two-day assembly service are separate options, not an automatic three-day turnaround. The combined schedule depends on available capacity, component readiness, and approved production files.
Have a fixed arrival date? Include it with your inquiry so production and shipping can be considered separately before you commit to the order.
What Inspection and Test Reports Will You Receive?
The most useful reports are those that help your team accept the boards and move to the next stage. That may mean confirming dimensions for installation, reviewing hidden solder joints, or checking that an LED assembly operates before system integration.
EBest’s PCB inspection services include electrical testing, AOI, X-ray inspection, and assembly quality checks. The methods and reports for your order can be agreed during quotation review.
These checks can help you assess the boards before acceptance:
Check
What it checks
Details to agree
Board electrical test
Continuity and isolation
Coverage and report format
Dimensions
Drawing compliance
Critical dimensions and tolerances
Assembly inspection
Placement and visible joints
Workmanship and critical features
X-ray, if needed
Hidden-joint inspection
Packages, criteria, and images
Functional test
Operation under test conditions
Test setup and pass/fail limits
Final checks
Cleanliness and delivery format
Residue, labels, and packaging
You can start by sharing your drawing and any existing acceptance checklist. For functional testing, we can review the power input, procedure, fixtures, and pass/fail limits with your team. The review can also cover panel or individual-board delivery and any medical-project records needed for the order and revision.
An LED operation check helps you verify board-level function. Thermal performance and service life require separate validation under the finished product’s operating conditions.
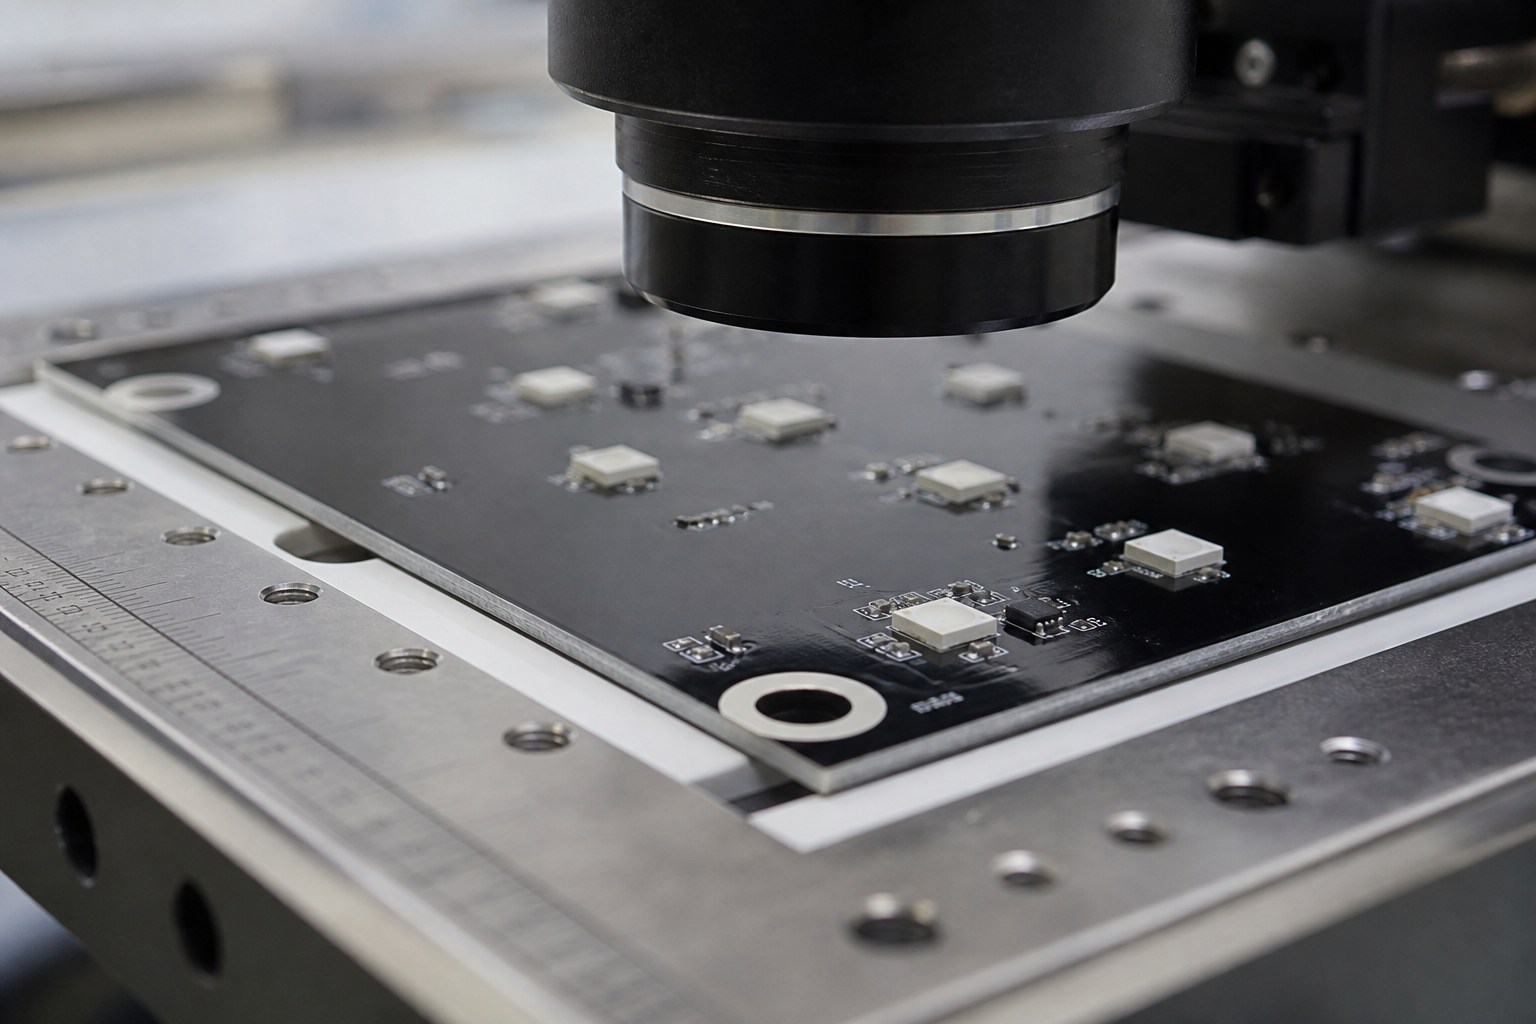
Illustrative optical inspection of board mounting-hole positions. AI-generated illustration.
IMS PCB PCBA Case Study: From Customer Requirements to Delivery
A surgical-lighting customer needed an assembled LED board, not just a bare aluminum PCB. EBest handled the aluminum-core board fabrication, component procurement, and SMT assembly, completing the project within 1.5 weeks.
The customer needed boards that could move on to installation in the lighting assembly. Alongside electrical operation, the order addressed LED placement, mounting-hole positions, and cleanliness—details that matter when the PCBA is fitted into the light.
The project at a glance:
Item
Details
Application
Surgical-lighting LED board
Construction
Single-sided aluminum-core PCB
Thickness
1.6 mm ±10%
Copper
1 oz
Finish
Lead-free tin
Mask / legend
Black / gray
Scope
PCB, component sourcing, SMT
Approval items
Panel data and stack-up
Completion
Within 1.5 weeks
Customer approval of the panel data and stack-up was required before production.
To help the LED board fit and function in the surgical-lighting system, we focused on four areas:
LED positions that follow the optical layout. The order highlighted LED placement offset, helping keep assembly focused on the positions in the customer’s approved design.
Mounting holes checked before installation. Optical measurement of hole positions was required before shipment to check alignment with the intended mounting points.
LED operation checked before system integration. The assembly instructions required all LEDs to be checked for operation before shipment, giving the customer a board-level check before installing the PCBA in the light.
Boards cleaned for delivery. The order specified cleaning and control of solder balls, rosin, and other residue as part of the delivery requirements.
This brought the bare board, purchased components, and assembly into one order, with linked PCB and SMT records and documented pre-shipment requirements. The completion time applies to this build; other projects are scheduled according to their specifications and component availability.
These checks covered the board, while the complete surgical light still needed its own optical, thermal, and lifetime validation.
For a similar lighting project, tell us where the board will be installed and which positions or dimensions are critical. We can review those details alongside your PCB and assembly files.
Surgical-lighting application illustration; not a photograph of the customer project. AI-generated illustration.
How Can You Request an IMS PCB Quote for Your Project?
You do not need every detail finalized before contacting us. Send your available PCB files, expected quantity, and whether you need bare boards or assembled boards. For assembly, include your current BOM if available. EBest can review the information and identify what else is needed to prepare your quote.
Start with what you have:
Available PCB files or drawings;
expected order quantity;
bare-board or assembly requirements;
target delivery date and destination.
Materials, component availability, and testing can be clarified during the review. If a part or material must remain unchanged, let us know so it stays central to the quotation. Before production, the fabrication files, BOM, placement data, and agreed acceptance requirements will need to be confirmed.
The quotation can separate fabrication, components, assembly, tooling, testing, and shipping where applicable, making it easier to see what you are paying for. Final pricing and lead time follow once the key requirements are confirmed.
Email your available project information to sales@bestpcbs.com. You can begin the conversation now and work through the remaining details during the review.
FAQs About IMS PCB PCBA Manufacturer
Can I order only the bare IMS PCB?
Yes. You can order bare boards and keep your existing assembly partner. EBest can review that partner’s panelization, finish, and handling requirements as part of the fabrication inquiry.
Can EBest purchase the components as well as manufacture the board?
Yes. You can bring fabrication, component sourcing, and assembly into one order. Your current BOM is a useful starting point; manufacturer part numbers and sourcing responsibilities can be clarified during review.
Can I supply selected components?
Yes, a mixed-sourcing arrangement can be reviewed for your project. Let us know which parts you want to supply, and we can review quantities, packaging, and arrival timing before finalizing the assembly schedule.
Can I request expedited IMS PCBA production?
Yes. Share your target arrival date and available files. EBest can review expedited options against board specifications, component availability, quantity, testing needs, and production capacity. The complete schedule is confirmed for your order, with shipping time identified separately.
Does a functioning LED board prove that the finished product meets its thermal requirements?
A working LED board confirms operation under the test conditions. To assess thermal performance in the finished light, a separate test needs to reflect the enclosure, cooling arrangement, and operating conditions.
Can you replace an unavailable component with an equivalent?
EBest can help identify alternatives for your review. Your team approves the replacement before purchase, keeping control of changes that may affect fit, performance, or reliability.
Looking for an IMS PCB PCBA manufacturer for your next build? Send what you have to sales@bestpcbs.com—whether that is a board drawing, a BOM, or an existing manufacturing package. EBest can help you take the next step toward a fabrication-and-assembly quote.
The latest Kingboard price increase concerns the materials used to manufacture PCBs, not an automatic increase in every finished-board quotation. An August 28, 2026 notice reproduced by financial media reports higher FR-4 and prepreg prices for newly accepted orders. For purchasing teams, the next step is to identify the material used in each board and confirm which commercial terms apply.
At EBest Circuit, we help customers review PCB material requirements alongside fabrication needs. This update explains the reported changes, where they enter a multilayer board’s material bill, and what to clarify when a supplier sends a revised quotation.
What Changed in the August 28 Notice?
Gelonghui’s August 28 report, carried by Sina Finance, reproduces a notice from Guangdong Kingboard Laminates Trading Co., Ltd. The stated adjustments are:
Material category in the notice
Reported increase
FR-4, all thicknesses
10%
Prepreg: 7628 and the notice’s thicker-cloth category
10%
Prepreg: the notice’s thin-cloth category below 7628
20%
The reproduced letter is dated August 28. We checked its wording against the report, but it was obtained through a media publication, not a direct supplier communication. Confirm the applicable grade and price with your material supplier before changing a purchase order.
When Does the New Pricing Apply?
The notice refers to new orders accepted from its issue date. It does not establish how every distributor will handle existing inventory, previously accepted orders, or an earlier quotation that remains valid.
Before approving a revised board price, ask for three specific confirmations:
Order status: Was the material order already accepted, or does the job still require a new purchase?
Quotation basis: Which material grade, copper weight, sheet size, quantity, currency, and tax basis are being compared?
Validity: How long does the revised quotation remain open, and what event fixes the price?
A finished-PCB purchase order and a laminate manufacturer’s order are different transactions. Do not assume that sending a board PO earlier automatically secures an earlier material price; obtain written confirmation from the party supplying your boards.
Why Are Glass Cloth and Copper Foil Important?
The letter cites rising prices and tighter supply of glass cloth and copper foil. Both are inputs to PCB laminate production; neither is simply an optional accessory that can be removed from a drawing.
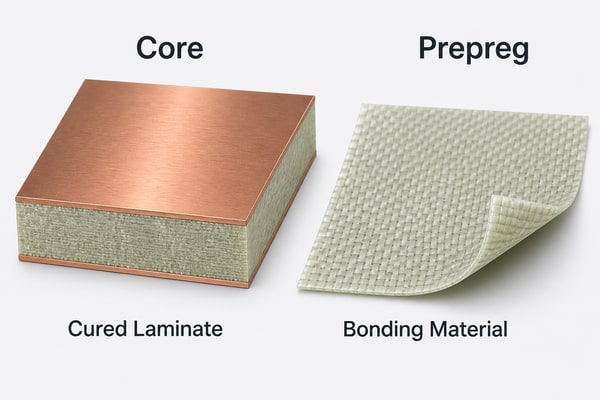
A copper-clad laminate combines a dielectric base with copper foil. Prepreg supplies resin-bearing reinforcement between layers during lamination. Their costs enter the material bill through different purchased items and constructions.
The notice alone does not tell us how much either input has risen across the entire market, how long supply pressure will last, or which next adjustment will follow. Those would require separate dated evidence. For a current order, the relevant information is the supplier’s quotation for the exact material being purchased.
PCB Prepreg vs Core: Which Material Is Affected?
The distinction in PCB prepreg vs core matters because a multilayer stackup uses cured laminate and bonding sheets differently. A core is already cured; prepreg starts as resin-impregnated reinforcement that bonds the assembly during pressing.
For background on the bonding stage, see our explanation of prepreg in PCB manufacturing. For this price review, identify the actual core and prepreg entries in the approved stackup rather than treating the entire board as a single sheet of FR-4.
When comparing prepreg PCB material, retain the manufacturer’s grade, resin system, glass style, resin content, and number of plies. Two options described simply as “FR-4 prepreg” may not have the same electrical properties or processing behavior. A purchasing description that omits these details can hide a construction change inside an apparently cheaper quotation.
Why Does Prepreg PCB Thickness Need a Construction Check?
Prepreg PCB thickness is not determined by a glass-style number alone. Resin content, the selected construction, and the pressed assembly all matter. Manufacturer data can list more than one thickness or resin-content option for the same glass style.
The notice’s wording around 7628 is a supplier pricing category. It should not be converted into a universal rule that every glass-style code with a smaller numerical value is physically thinner. Match each ordered prepreg item to the supplier’s classification.
Construction also affects PCB prepreg dielectric constant. Isola’s laminate-manufacturing guide explains that glass construction and retained resin content influence dielectric properties. Its material data illustrate why an apparently similar glass designation is not enough to prove equivalence; those Isola values should not be copied into a Kingboard design.
For an impedance-controlled board, changing dielectric spacing or material properties can require a new impedance calculation and an approved stackup revision. Keep the electrical requirement fixed while evaluating the material choice.
Does a 20% Prepreg Increase Mean a 20% PCB Price Increase?
No. A percentage applied to one purchased material does not automatically apply to the total selling price of a finished PCB. The board also includes other materials, fabrication operations, inspection, testing, handling, and commercial terms.
A useful calculation starts with the affected material lines, not the total board invoice: multiply each old material-line cost by its applicable adjustment, then add the differences. That estimates the change in those lines only, assuming the same specification, quantity, and purchasing basis.
It still does not determine the final commercial quotation. Inventory purchased at an earlier price, panel utilization, production volume, and other cost changes may affect the outcome. Our copper-clad laminate price guide provides broader background on material-price factors.
If a revised quotation cites the Kingboard price increase, ask which material lines changed and whether the board specification stayed the same. A traceable explanation is more useful than applying a headline percentage to every item.
Which Cost-Saving Changes Need Engineering Approval?
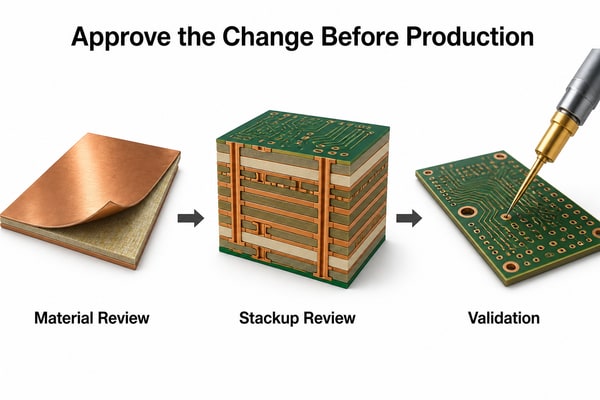
Start with options that preserve the approved design, such as reviewing order quantities or panel utilization with the fabricator. Material substitutions require a separate technical decision; a lower material price does not establish that the replacement will work.
Changing prepreg construction: Review finished dielectric spacing, resin availability around copper features, and electrical requirements.
Changing laminate grade: Compare the relevant thermal and electrical properties and any material restrictions on the drawing.
Reducing copper: Recheck current handling, thermal behavior, and fabrication requirements rather than treating copper weight as a purchasing-only choice.
Changing a qualified build: Agree on required samples, inspection, and customer approval before production release.
Keep the existing approved construction if equivalence has not been demonstrated or the customer does not permit substitutions. Requalification time and scrap risk can outweigh a small purchase-price saving.
How Can We Help You Review a Material-Cost Change?
At EBest Circuit, we provide PCB fabrication and PCBA services with technical support for material and build requirements. We can review your approved stackup and discuss which material choices are fixed, which alternatives may be evaluated, and what information is needed for a current quotation.
Send your Gerber files, stackup, specified laminate grade, copper weight, order quantity, and required delivery date to sales@bestpcbs.com. If you are comparing a revised quote, include the earlier specification and quote date so we can compare the same build. Any proposed material change should be documented and approved before manufacturing.
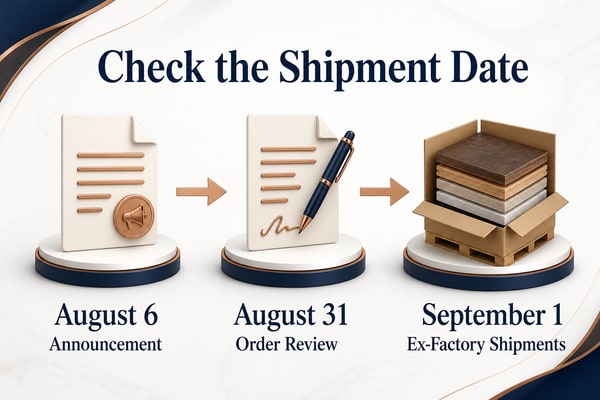
The Panasonic laminate price increase announced on August 6, 2026 takes effect for September 1 shipments on an ex-factory basis. This August 31 update is an execution reminder, not a new price announcement. The change covers several circuit-board material categories, with different rates for general glass-epoxy and low-loss products.
For PCB buyers, the practical questions are which material their approved build uses, when that material ships, and whether a revised quotation still describes the same board. At EBest Circuit, we can review those technical requirements with you before a proposed substitution changes the build.
Which Panasonic PCB Materials Are Included?
Panasonic Industry’s official notice lists the following changes from current material prices:
Material group
Affected products
Increase
General multilayer glass epoxy
Laminate and prepreg
30%
MEGTRON / XPEDION
Laminate and prepreg
15%
LEXCM GX substrate materials
Laminate and prepreg
30%
CEM-3
Glass-composite materials
30%
FCCL
Flexible circuit-board materials
15%
These are Panasonic PCB materials, not replacement control boards for air conditioners or other appliances. Package-substrate materials, flexible materials, and ordinary rigid-board materials should also remain separate entries in a purchasing review. A rate for one category should not be applied to another simply because both are used somewhere in electronics manufacturing.
When Does the September Revision Take Effect?
The stated trigger is shipment from the factory from September 1, 2026. It is not described as a deadline based only on when a customer submits a purchase order.
For a board buyer, the laminate shipment date, PCB production start, and finished-board delivery date are three different milestones. Ask the fabricator which material transaction applies to your order rather than inferring it from your requested PCB delivery date.
Material already allocated: Confirm the allocation, quantity, and applicable quotation in writing.
Material still to be purchased: Obtain a current quote and an expected material shipment date.
Repeat orders or scheduled releases: Check whether each release has its own purchasing and pricing conditions.
A quotation’s validity period is not the same as a stock reservation. If the supplier cannot confirm allocation, do not treat material availability or an earlier price as secured.
Why Is Panasonic Revising Material Prices?
Panasonic cites sustained increases in principal raw materials, together with elevated auxiliary-material, energy, logistics, and other costs. The notice presents the revision as necessary to support continued supply.
That explanation does not provide a PCB-fabricator cost breakdown. A board quotation includes more than the purchased laminate and bonding sheets. The affected material share, processing route, quantities, and contractual terms must be reviewed for the specific order; no finished-PCB price increase can be calculated from the announcement alone.
Nor does a price notice establish that every material grade is unavailable. Treat price, stock allocation, and lead time as separate questions. A higher price is not proof of an earlier delivery slot, and an available sample sheet is not proof of production-volume availability.
What Does This Mean for Panasonic MEGTRON 6 and 7?
Panasonic MEGTRON 6 and Panasonic MEGTRON 7 are material families used in high-performance multilayer boards. They should be identified by the exact laminate and prepreg grades on the approved stackup, not just the family name.
A common percentage adjustment does not make two grades equal in absolute price or technically interchangeable. Their earlier prices, constructions, and processing requirements can differ. A purchasing comparison must retain the grade suffix, copper foil, dielectric construction, panel requirements, and order volume.
For high-speed designs, changing the dielectric system is a signal-integrity decision as well as a cost decision. Channel loss and impedance depend on the board construction and routing, not on the material trade name alone. Our high-speed PCB design guidance explains why the full interconnect needs attention.
If the drawing explicitly specifies a manufacturer and grade, keep that requirement in the quote. Present any alternative as a separate option requiring approval, not as an equivalent silently substituted during purchasing.
What Should You Check in a Panasonic MEGTRON 6 Datasheet?
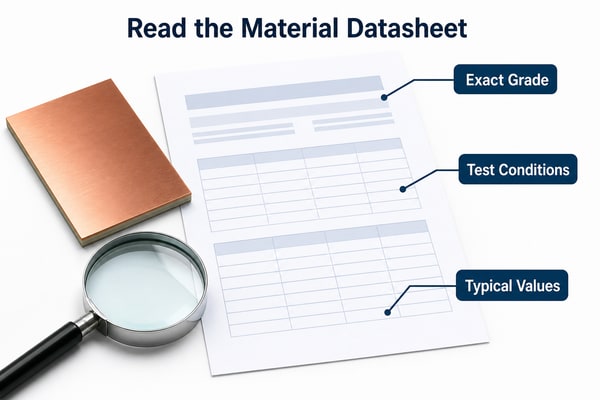
A Panasonic MEGTRON 6 datasheet is useful for confirming which product a quotation actually refers to. The manufacturer’s documentation distinguishes laminate variants such as R-5775(N), R-5775(K), and R-5775(G), with corresponding R-5670 prepregs. It also identifies typical values and the conditions used to measure them.
Exact product: Match the complete grade and suffix, including the associated prepreg.
Electrical data: Compare Dk and Df only with their frequency, method, and sample conditions stated.
Thermal data: Check that the property and test method match the assembly requirement being evaluated.
Copper and construction: Retain the specified foil and dielectric details when comparing transmission performance.
Do not take a typical datasheet result as a guaranteed acceptance limit for every finished board. Define the relevant build and inspection requirements separately. For the role of the bonding material, our PCB prepreg overview provides a useful starting point.
Can a Different Laminate Reduce Cost Without Changing Performance?
Possibly, but that requires evidence for the actual design. A material with a lower quoted sheet price can still require a stackup change, trace-width adjustment, process review, or additional qualification.
Start by fixing the performance and customer requirements that cannot change. Then compare candidate materials against those requirements, estimate the work needed to approve the change, and obtain written customer acceptance before release.
Our stackup and impedance-control guidance is relevant when dielectric thickness or properties change. Price comparisons should not leave the stackup as an unspecified item to be decided after ordering.
Keeping the existing material may be the better choice when a product is already qualified, the delivery window cannot accommodate validation, or the expected saving is smaller than the change effort. The purpose of a review is to make that tradeoff visible, not to assume that a substitute is always available or worthwhile.
What Should Be Confirmed for September Deliveries?
Ask for a written order confirmation that connects the material, price, and schedule. “Material available” is too broad if the required grade, thickness, copper foil, or quantity is still unresolved.
Approved laminate and prepreg part numbers, plus any permitted alternatives.
The material allocation and expected factory shipment relevant to your job.
The quotation date, validity, and treatment of scheduled releases.
The expected PCB delivery date after material receipt and fabrication.
Who approves a material change and what validation is required.
When discussing the Panasonic laminate price increase internally, keep the supplier’s material notice separate from your project’s board quotation. That gives engineering and purchasing the same documented basis for approval.
How Can EBest Circuit Help With Your Material Review?
At EBest Circuit, we support PCB fabrication and PCBA projects, including multilayer and high-speed board requirements. We can review your specified materials and stackup, clarify which requirements must remain fixed, and discuss alternatives that may merit engineering evaluation.
Email sales@bestpcbs.com with your Gerber files, approved stackup, full laminate and prepreg grades, quantities, and target delivery date. Include any customer restrictions on substitution. We will use those requirements to discuss a current quotation and the review needed before changing the build, without treating a material-price headline as a finished-board price.
Choose a metal core PCB manufacturer in the USA by matching the released construction, evidence package, quantity profile, and assembly scope to the factory that will build the order. A suitable manufacturer must be able to control the specified metal base, dielectric, copper, hole isolation, mechanical features, surface finish, and assembly interface as one design.
Shortlist suppliers by project fit and order evidence. Confirm who will manufacture the board, which material and process route will be used, what records will accompany the order, and whether those controls remain stable from prototype through repeat production. This keeps the selection process focused on a manufacturable, verifiable board rather than a long list of unrelated capabilities.
What Should You Verify Before Shortlisting a Metal Core PCB Manufacturer Serving the USA?
Start with eight selection factors that determine whether a supplier can support the complete order. Remove candidates that cannot match the construction, evidence, quantity, or assembly scope before engineering time is spent on detailed quotations.
Relevant production history: Ask for evidence of work with the same MCPCB construction; standard single-sided aluminum experience does not qualify every metal-core build.
Metal-base range: Confirm the supported aluminum alloys, copper bases, thicknesses, and any special bonded or machined structures.
Thermal material control: Review dielectric grade, thickness, thermal performance, electrical isolation, and substitution policy together.
Custom construction capability: Match plated holes, multilayer bonding, pockets, routing, countersinks, and other drawing features to the proposed factory.
Order-level quality evidence: Define material, dimensional, electrical, isolation, and traceability records that will be released with the lot.
Assembly integration: If PCBA is required, check whether fabrication, soldering, heat-sink interfaces, inspection, and test ownership are coordinated.
Quantity fit: Confirm prototype support, intended production capacity, tooling, material availability, and repeat-order controls.
DFM response: A useful review identifies a specific drawing, material, isolation, machining, or assembly risk and returns a clear decision or question.
Which Metal Core PCB Construction Must the Manufacturer Prove?
Approve a supplier across the independent construction axes used by your design, because “metal core PCB” does not describe one manufacturing route. Separate the base material, circuit-layer structure, thermal-path architecture, electrical specialization, and mechanical integration before checking factory experience.
Base material axis: For aluminum, verify alloy, thickness, laminate, profiling, and panel control; for copper, add source control, weight, oxidation protection, machining, and handling.
Circuit-layer axis: A single-sided IMS route differs from a plated double-sided or multilayer route. Confirm hole isolation, bond sequence, registration, stackup limits, and internal-construction evidence as applicable.
Thermal-path axis: Distinguish a conventional dielectric-based path from a direct thermal path. Require a cross-section that shows both heat flow and electrical isolation.
Electrical-specialization axis: Power and LED IMS work emphasizes thermal and assembly control, while RF metal-backed work adds RF laminate handling, bond film, pockets, metal-carrier plating, dimensional datums, and finish compatibility.
Mechanical-integration axis: Separate a standard profiled base from a precision-machined carrier. Direct mounting to a heat sink, housing, or frame brings outline, holes, flatness, burr, pocket, and mounting surfaces into supplier qualification.
A supplier experienced with single-sided LED aluminum boards may still lack the plated, multilayer, direct-path, RF, or precision-machining controls required by another design. Ask the candidate to mark each axis as routine, conditional, or outside its current process window.
Which MCPCB Specifications Should You Confirm Before Choosing a Manufacturer?
Match the required stackup to a confirmed factory process window before approving a supplier. Best Technology publishes the following reference values in its single-layer MCPCB data and current product catalog. Use them for initial quotation screening. Only a build-specific review can confirm whether the required material, copper, geometry, thickness, layer count, and panel size can be produced together.
Capability item
Best Technology reference range
What to confirm for the order
Single-layer base material
Aluminum, copper, or iron alloy
Exact alloy, metal thickness, source, surface treatment, and whether the quotation uses the named material
Single-layer dielectric conductivity
0.8, 1.0, 1.5, 2.0, or 3.0 W/(m·K)
Material manufacturer and grade, dielectric thickness, thermal resistance, dielectric strength, and substitution rule
Copper weight
0.5, 1.0, 2.0, or 3.0 oz; up to 10 oz is listed
Finished copper, minimum line/space at that weight, etching tolerance, and inspection method
Single-layer board thickness
0.5–3.0 mm
Finished-thickness tolerance, flatness, mounting interface, and panel handling
General MCPCB layer count
1–10 layers
Released cross-section, plated-hole isolation, lamination sequence, registration, and factory history with that structure
General MCPCB board thickness
0.8–5.0 mm
Whether the requested thickness is valid with the selected layer count, metal base, copper, machining, and panel size
Minimum line/space
4/4 mil, or 0.10/0.10 mm
Applicable copper weight, conductor tolerance, annular features, and production inspection basis
Send the same drawing, cross-section, quantities, and evidence requirements to every shortlisted supplier. Require the quotation to identify which values are routine, which require engineering review, and which combinations are unavailable at the named factory.
How Do You Verify the Manufacturer’s Quality and Traceability?
Reliability is demonstrated when the supplier can connect its quality system to your material, revision, lot, tests, and changes. Verify the certificate’s legal entity, site, and scope, then require order-specific material, revision, lot, test, and change records.
Site and scope: Check the legal entity, factory address, certificate scope, and actual operations used for the proposed order.
Incoming materials: Confirm how the metal base, thermal laminate, copper, solder mask, and finish materials are identified and released.
Process traceability: Ask how work orders, material lots, inspection results, deviations, and final shipments remain linked.
Electrical controls: Define the net test and any isolation requirement with the test method, voltage or limit supplied by the approved specification.
Dimensional controls: Identify which holes, cutouts, thicknesses, flatness points, and datums receive recorded inspection.
Nonconformance handling: Require segregation, disposition authority, corrective action, and customer notification for deviations that affect fit or performance.
Change control: Specify which material, process, factory, tooling, or sub-supplier changes require approval before the next lot.
The useful output is a qualification record that states what was verified, what remains conditional, and which documents will be delivered with production. Avoid approving a supplier from a logo sheet or questionnaire that is not connected to the actual build route.
How Do Material and Thermal Controls Affect Supplier Qualification?
Select a manufacturer whose routine materials and process controls match the metal base already justified by the thermal, mechanical, electrical, and cost design. Material selection comes first; supplier qualification then verifies the factory controls needed for that base and construction.
For an aluminum PCB project
Material identity: Confirm the base alloy, thickness, approved thermal laminate, dielectric thickness, and substitution limits.
Profiling control: Review routing, punching where applicable, V-scoring, burr control, and panel-to-board flatness.
Repeatability: Ask how thermal material and base-metal lots are controlled across prototype and production orders.
For a copper core PCB project
Base handling: Confirm copper-base weight, sourcing, oxidation protection, machining, and in-process handling.
Construction complexity: Review bonding, direct-path features, plated isolation, pockets, and registration with a cross-section.
Commercial impact: Ask the supplier to separate material, machining, tooling, yield-sensitive features, and assembly costs in the quote.
Do not assume that a high-volume aluminum IMS line can automatically produce a copper pedestal, plated metal-core, or RF metal-backed design. Qualification follows the released structure, not the broad MCPCB category.
Which Thermal Material Records Should the Supplier Provide?
Thermal material must be compared as a system because conductivity alone does not define heat flow or insulation performance. Two laminates with the same nominal W/m-K value can use different dielectric thicknesses and therefore produce different thermal resistance and electrical margins.
Thermal conductivity: Record the published value, test basis, and grade instead of accepting an unlabeled number.
Dielectric thickness: Confirm the finished or nominal thickness used in the thermal and isolation assessment.
Thermal resistance: Compare the full dielectric path and relevant area instead of using the material conductivity headline by itself.
Dielectric strength: Tie the required electrical isolation to an approved test method and design margin.
Material identity: Lock the manufacturer, grade, and accepted equivalent route when consistency matters.
Substitution policy: Require approval before a supplier changes grade, thickness, or source, even if the nominal conductivity is unchanged.
A strong candidate can return an approved stackup or material proposal that shows the copper, dielectric, and metal-base relationship. A weak candidate quotes “2 W/m-K” or “3 W/m-K” without naming the grade, dielectric thickness, isolation basis, or substitution boundary.
Can the Manufacturer Control Both Mechanical Fit and PCB Assembly?
Mechanical capability can disqualify an otherwise suitable MCPCB supplier when the board mounts directly to a heat sink, housing, or structural frame. Control the metal base as both a precision interface and a thermal layer.
Outline and datums: Define the dimensions that locate the board in the final assembly and the datum scheme used for inspection.
Slots and cutouts: State size, position, corner-radius, and burr requirements that affect clearance or fit.
Countersinks and countersunk holes: Specify side, angle, final diameter, depth, plating status, and relationship to the mounting hardware.
Routing and V-scoring: Confirm the separation method, residual thickness where relevant, edge quality, and component-to-edge constraints.
Flatness: Define the measurement condition and acceptance limit for the bare board or assembled board, whichever controls fit.
Mounting holes: Identify electrical isolation, annular clearance, tolerance, and any metal exposure requirement.
Surface contact: Mark heat-sink interfaces, keep-out areas, thermal interface material, and cosmetic or conductive surfaces on the drawing.
Ask the supplier which features are measured, with what fixture or datum, and whether the result is recorded. A drawing that says “fit to heat sink” without measurable criteria cannot produce a comparable supplier decision.
How Should Assembly Capability Be Verified?
Choose an assembly-capable manufacturer when fabrication choices and the soldering or mounting process share the same thermal and mechanical risks. The evaluation should connect the bare-board design to component placement, reflow, heat spreading, attachment, and test access.
High-power components: Review pad geometry, copper spreading, void-sensitive thermal pads, component limits, and inspection access for LEDs, MOSFETs, IGBTs, or similar devices.
Soldering process: Confirm the assembly profile is compatible with the laminate, finish, board mass, component set, and approved materials.
Heavy components: Check support, handling, depaneling, connector loads, and any secondary mechanical attachment.
Thermal interface: Define the heat sink, interface material, mounting hardware, torque source, cleanliness, and flatness assumptions when they are part of the order.
Inspection plan: Select AOI, X-ray, solder-joint inspection, or other methods only where the component and joint geometry make them useful.
Test ownership: State whether the supplier performs bare-board electrical testing, assembly inspection, programming, functional testing, or customer-defined verification.
If fabrication and assembly are split between suppliers, assign responsibility for material storage, solder-profile approval, thermal interface preparation, board damage, and failure analysis. The lowest bare-board price can lose value when those interfaces are unmanaged.
Which Tests Should Be Included in the Manufacturer’s Release Package?
The test package should verify the risks created by the released construction and drawing. Not every order requires every test, so define the method, sample or lot coverage, acceptance basis, and record before comparing suppliers.
Electrical test: Verify opens and shorts against the released net data using the agreed coverage and acceptance rules.
Isolation test: Apply the approved method where conductors, plated holes, mounting features, or direct-path structures must remain isolated from the metal base.
AOI: Use image inspection for applicable conductor, pad, and solder-mask features while recognizing that it does not replace electrical or internal construction evidence.
Dimensional inspection: Record critical outlines, holes, slots, countersinks, thicknesses, and datums that control assembly fit.
Flatness inspection: Define support condition, board state, measurement points, and limit before treating a result as comparable.
Material verification: Link the approved dielectric and metal base to the received lot and production traveler.
Microsection: Use it when plated, bonded, multilayer, or isolation features require internal construction evidence.
Solderability or finish evidence: Specify it when shelf life, assembly process, contact use, or a customer requirement makes the result relevant.
For any temperature or thermal comparison, define input power, sensor position, ambient condition, heat sink, thermal interface material, mounting force, stabilization time, and board revision. Results measured under different conditions should not be used to rank suppliers.
Can the Manufacturer Maintain the Same Controls from Prototype to Volume?
A prototype supplier is suitable for volume only when the intended factory, material route, tooling, controls, and change process can scale with the order. Treat a successful sample as evidence for that build only; volume approval requires the intended production route and repeat-order controls.
Prototype objective: Close DFM questions and verify thermal, electrical, mechanical, assembly, and test interfaces before the design is frozen.
Material availability: Identify whether the prototype uses stocked material, a temporary substitute, or the intended production grade.
Tooling route: Record temporary and production tooling differences for profiling, fixtures, stencils, inspection, and test.
Pilot evidence: Use the intended process route and review representative material, dimensional, electrical, isolation, and assembly records.
Production release: Freeze the approved data, factory, material, substitution limits, test scope, packaging, and change-notification rules.
Repeat-order control: Compare each new lot against the released revision and approved deviations rather than relying on the previous purchase order alone.
Ask who owns the transfer from engineering samples to production and what must be requalified if the factory, material, tooling, or assembly route changes. This answer is often more useful than a broad annual-capacity figure.
How Should You Compare Quotes from MCPCB Manufacturers Serving the USA?
Compare price only after every supplier has quoted the same construction, quantity, evidence, responsibility, and delivery basis. Otherwise, a lower total may reflect a thinner dielectric, different metal base, relaxed tolerance, reduced testing, excluded tooling, or a different assembly scope.
Quote field
Equal-scope check
Materials
Same dielectric grade or approved equivalent, thickness, conductivity basis, metal type, and base thickness
Copper and stackup
Same copper weights, layer construction, finished thickness, and plated or isolated features
Mechanical scope
Same outline, slots, holes, countersinks, flatness, burr, tolerances, and tooling assumptions
Finish and marking
Same surface finish, solder mask, legend, exposed metal treatment, and packaging requirements
Inspection and tests
Same electrical, isolation, dimensional, construction, assembly, and reporting scope
Assembly responsibility
Same component sourcing, stencil, placement, soldering, inspection, programming, functional test, and rework boundary
Commercial basis
Same quantity, tooling treatment, delivery point, freight, duties, payment terms, and production site
Use one comparison sheet for every metal core PCB manufacturer in the USA that reaches the final shortlist. Mark assumptions and exclusions explicitly, then ask each supplier to close the gaps before the commercial decision.
Which Supplier Red Flags Should Stop or Delay Approval?
Reject or hold a supplier when its quote hides the material, process, evidence, or change boundary that controls your design. Each red flag below creates a specific downstream risk.
No material grade: A quote that says only “aluminum PCB” or “3 W/m-K” permits unknown dielectric identity and inconsistent substitutions.
Conductivity without thickness: The thermal path cannot be compared when dielectric thickness and thermal resistance are missing.
No hole-isolation answer: Plated or mounting features near the metal base may create electrical failure or an unbuildable stackup.
Unexplained low price: A large price difference may come from different materials, tolerances, testing, tooling, production sites, or excluded services.
Prototype-to-volume material change: The approved sample may not represent the production board if grade or supplier changes are uncontrolled.
Undefined test scope: “100% tested” has little value without naming the test, coverage, method, limit, and record.
No traceability: Material, traveler, test, and shipment records cannot support containment or root-cause analysis when lots are not linked.
No DFM response to unusual features: Silence on countersinks, pockets, isolated holes, tight flatness, or thermal-interface details may indicate that the supplier has not reviewed the actual construction.
Do not treat one red flag as an automatic rejection when the supplier can clarify and document the point. The decision should record the closed answer, any approved exception, and the evidence required before production release.
What Should a USA-Bound MCPCB RFQ Include?
A quote-ready package must define the electrical data, stackup, thermal material, mechanical interface, quantity, assembly scope, and evidence expectations. Sending this information together reduces assumptions and makes supplier responses comparable.
Electrical fabrication data: Gerber or ODB++, NC drill files, netlist where available, board revision, and fabrication drawing.
Cross-section: Copper weights, dielectric grade and thickness, metal type and thickness, finished thickness, and layer sequence.
Thermal and isolation requirements: Thermal property basis, dielectric strength or isolation requirement, direct-path details, and approved test conditions.
Finish and marking: Surface finish, solder mask, legend, exposed metal surfaces, special cleanliness, and packaging needs.
Order profile: Prototype quantity, pilot quantity, volume forecast, delivery location, requested production site, and trade terms.
Assembly data: BOM, pick-and-place file, assembly drawing, approved component alternatives, stencil or soldering constraints, and heat-sink interface details.
Verification package: Required electrical, isolation, dimensional, construction, assembly, programming, functional-test, traceability, and change records.
Send the controlled package to sales@bestpcbs.com and request a free DFM review plus a quotation that states the proposed material, construction, open questions, inspection scope, assembly responsibility, and delivery basis.
Why Choose EBest Circuit for USA-Bound Metal Core PCB Projects?
EBest Circuit gives US buyers one engineering and commercial interface for metal-core fabrication, assembly planning, inspection scope, and repeat-order control. EBest is a China-based source manufacturer, so every quotation should identify the manufacturing origin, proposed construction, evidence package, and delivery basis clearly.
Construction-specific review: Aluminum, copper-base, plated, multilayer, direct-path, and machined structures are reviewed against the released cross-section and drawing.
Published capability references: The supplier can begin with concrete material, conductivity, copper, thickness, geometry, and size values, then identify which combinations require engineering review.
Free DFM review: Drilling, hole isolation, routing, machining, flatness, thermal-interface, and assembly questions can be closed before quotation release.
PCB and PCBA coordination: Fabrication, component sourcing, SMT/THT assembly, inspection, and project-specific test responsibilities can be defined in one order scope.
Prototype-to-production control: Material identity, drawing revision, approved deviations, inspection requirements, and change-notification rules can remain linked to repeat orders.
Quote transparency: The quotation can state assumptions, exclusions, tooling, evidence, assembly responsibility, manufacturing site, and delivery terms for an equal-scope comparison.
Send the controlled design package to sales@bestpcbs.com for a construction review and a quote that identifies open technical decisions before production.
FAQs About Selecting a Metal Core PCB Manufacturer for the USA
Q1: Does a US sales office mean the board will be manufactured in the USA?
A1: No. Ask for the physical factory address and the operations performed there, including imaging, etching, drilling, bonding, profiling, finish, and electrical test where relevant. Put any country-of-manufacture requirement in the RFQ, supplier response, and purchase documentation so the order does not depend on a sales-address assumption.
Q2: Should I ask for a sample before approving an MCPCB supplier?
A2: Use a sample that represents the intended material and process route. A generic sample may show workmanship, but it does not qualify your dielectric, metal base, isolation, machining, or assembly interface. Record which features the sample proves and which items still require first-article or pilot evidence.
Q3: Can a supplier substitute a thermal laminate with the same W/m-K rating?
A3: Only after technical review and approval. Check dielectric thickness, thermal resistance, dielectric strength, adhesion, assembly compatibility, availability, and change records before accepting an equivalent. Require the supplier to identify the proposed grade and explain which released requirements remain unchanged instead of approving it from conductivity alone.
Q4: When should I request a microsection?
A4: Request one when internal construction evidence affects release. Plated holes, multilayer bonding, isolated features, or a customer requirement may justify a representative microsection. Define the sampled feature, lot or panel relationship, preparation method, acceptance basis, and record retention before treating the image as production evidence.
Q5: Is an audit always required before placing an MCPCB order?
A5: Use risk to set the qualification depth. A document review may suit a low-risk prototype, while restricted, high-volume, safety-relevant, or complex constructions may require deeper site and process evidence. Base the decision on construction complexity, consequence of failure, supply continuity, required origin, and the records available from the named factory.
Q6: What should be frozen after the prototype is approved?
A6: Freeze the released data and the variables that affect equivalence. These normally include the factory, material grade, cross-section, critical drawing notes, test scope, approved deviations, and change-notification rules. Also identify temporary prototype tooling or substitutions so they are not silently carried into the production baseline.
Q7: How should I handle an unusually low quotation?
A7: Run an equal-scope comparison before negotiating price. Check materials, thicknesses, tolerances, tests, tooling, assembly exclusions, quantities, delivery terms, and build site. Ask the supplier to confirm every exception in writing; the remaining difference is then a commercial choice rather than an unidentified technical reduction.
Q8: Can an MCPCB supplier use separate fabrication and assembly factories?
A8: Yes, if ownership and change control are explicit. The quote should name each site and assign responsibility for materials, solder profiles, handling damage, inspection, failures, and corrective action. Confirm who approves fabrication changes and who leads containment when a defect could have originated at either site.
Q9: What evidence should be retained for repeat orders?
A9: Retain the approved revision and lot-linked release records. Material identity, deviations, critical inspection, electrical or isolation results, shipment identity, and approved changes support later comparison and containment. Keep the supplier’s production-site and substitution approvals with the same order identity so a repeat build can be checked against the actual baseline.
Q10: When is a one-stop PCB and assembly supplier useful?
A10: It is useful when fabrication and assembly decisions share the same thermal or mechanical interface. Confirm that one owner coordinates the stackup, soldering process, component risks, heat-sink interface, inspection, and test scope. The quotation should also name the factory and responsible owner for every required process.
Choosing among HDI PCB manufacturers in UK requires more than finding a supplier that lists “HDI” on a capability page. The right manufacturer must review your actual buildup, explain how each microvia is formed and filled, identify the proposed production site, and show how the released construction will be controlled from prototype through repeat orders.
Start with the features that create manufacturing risk: microvia layer pairs, stacked or staggered structures, via-in-pad, lamination cycles, finished copper, fine features, material system and impedance requirements. Then compare suppliers using the same files, quantities, inspection scope and delivery assumptions. This exposes incomplete quotations early and turns a general supplier search into a defensible manufacturing decision.
How to Choose an HDI PCB Manufacturer in UK?
Choose an HDI PCB manufacturer in UK by matching the proposed factory, process controls and evidence package to your board. A UK address may represent a fabrication site, sales office, managed supply service or assembly provider, so the quotation should name where the bare board will be produced and which operations are subcontracted.
Match the buildup: submit the layer stack and microvia start/stop layers so the supplier cannot silently simplify the routing concept.
Confirm materials: identify the laminate family, electrical properties and acceptable substitutions because changes can alter impedance and pressing behavior.
Check prototype and production routes: ask whether both use the same site, materials and critical processes; define approval for any transfer.
Agree on evidence: specify electrical test, microsection, impedance verification, inspection reports and lot records before comparing prices.
Evaluate assembly ownership: for BGA, CSP or via-in-pad designs, determine how bare-board findings return to the assembly team.
Judge communication by output: a useful supplier returns a marked-up stackup, DFM questions, deviations and an evidence plan—not only a quick reply.
What Capabilities Should HDI PCB Manufacturers in UK Provide?
Look for capabilities that correspond directly to routing, component, signal-integrity and reliability requirements. Minimums depend on layer count, copper weight, material, panel size and volume.
HDI process capability
Published UK capability example
Maximum layer count
Up to 32 layers
Laser microvia diameter
Down to 75 µm
Mechanical drill diameter
Down to 0.105 mm
Fine track and gap
Down to 50 µm
Microvia aspect ratio
Up to 1:1
Sequential lamination
Up to 6 lamination cycles
Supported via structures
Blind, buried, stacked and staggered microvias
Via filling
Copper-filled and resin-filled vias
Controlled impedance
±10% standard; ±5% advanced capability
Electrical test
100% electrical test
The numerical examples above are currently published by Exception PCB for its UK HDI production environment; Rush PCB UK separately publishes up to 20+ layers, 0.1 mm microvias and 50/50 µm trace/space. These are screening references, not universal limits for all HDI PCB manufacturers in UK. Require the shortlisted factory to return values tied to your material, copper, panel and volume.
How Can You Verify a Reliable HDI PCB Manufacturer in UK?
A reliable manufacturer connects each important claim to a site-specific process, review record and acceptance method. Certificates may support qualification, but they do not prove that a particular microvia stack has been assessed.
Build-specific DFM: require comments tied to actual layer pairs, microvia spans, copper, materials and tolerances. A generic “approved” response does not show that the construction was reviewed.
Named production site: record the physical factory and which processes it performs. If laser drilling, filling or testing is subcontracted, require the responsible site and control method.
Material traceability: record manufacturer, grade and lot identity, and require approval before substitution. This protects impedance and lamination behavior from unreviewed changes.
Microvia evidence: agree on microsection locations, plating and fill criteria, sampling frequency and the report supplied with the order.
Electrical and impedance testing: define the source netlist, test coverage, coupon design, target tolerance and report format rather than accepting “tested” as a complete answer.
Registration control: ask how sequential-lamination registration is monitored and what evidence demonstrates that capture pads and interlayer alignment meet the drawing.
Prototype-to-production consistency: confirm whether the same stackup, material, factory and critical process route will be used after prototype approval.
Change and nonconformance control: define which changes need written approval and who owns containment, root-cause analysis and corrective action after fabrication or assembly.
Request report samples before ordering. This proves the evidence is part of the operating process rather than a document requested after the boards are finished.
Why Choose EBest as an Alternative to HDI PCB Manufacturers in UK?
When UK production is not a contractual requirement, EBest Circuit offers a China-based route that connects HDI fabrication, engineering review and PCB assembly. EBest is not presented as a UK manufacturer; it is an alternative for UK projects needing coordinated overseas manufacturing.
Build-specific review: stackup, microvia map, via-in-pad, materials and impedance are reviewed against the intended construction.
DFM before production: Gerber or ODB++, drill data and notes are checked for ambiguous transitions, conflicts and avoidable complexity.
Fabrication and assembly coordination: board production, sourcing, SMT, inspection and test can share one project workflow.
Prototype-to-volume control: approved data, revisions and deviations can be retained for later builds.
Project-defined evidence: electrical test, AOI, microsection, impedance and assembly inspection are scoped to the design.
Pre-quotation support: unresolved manufacturing and assembly questions are identified before commercial comparison.
Send Gerber or ODB++, stackup, drill files and project requirements to sales@bestpcbs.com for a free DFM review and quotation.
How Should You Compare Quotes From HDI PCB Manufacturers in UK?
Compare quotations only after every HDI PCB manufacturer in UK has priced the same construction, production route and acceptance evidence. Use the following checks:
Freeze the technical baseline: use one released stackup, via map, material requirement, copper weight, surface finish and impedance table. Otherwise, a lower quote may represent a simpler board.
Separate setup from unit price: identify tooling, engineering, coupons and one-time test charges so repeat-order cost is visible.
Confirm the buildup assumption: require the quoted lamination cycles and stacked/staggered microvia treatment in writing because they are major cost drivers.
Check included evidence: state whether electrical test, impedance reports, microsections, first-article records and certificates are included or charged separately.
Identify the production site: compare UK-built, UK-managed and overseas manufacture honestly; include freight, import handling and any transfer risk.
Normalize quantity and delivery: request the same prototype, pilot and repeat-order quantities with the same delivery point and required date.
List every deviation: a quote that substitutes material or omits a process is not comparable until the difference is reviewed and accepted.
Which Design Choices Increase Quotes From HDI PCB Manufacturers in UK?
Design choices increase cost when they add process cycles, reduce yield or require tighter verification. DFM can reduce those costs without weakening function.
Extra buildup cycles: each adds pressing, drilling, imaging and registration work.
Stacked microvias: use them for necessary vertical transitions; staggered structures may be simpler when routing permits.
Filled and capped vias: restrict them to locations that require pad escape, thermal or assembly performance.
Fine features: review local bottlenecks instead of applying an extreme rule across the board.
Specialty materials: specify performance needs and permitted alternatives to avoid unnecessary sourcing constraints.
Inspection: connect each extra record or test to a real risk and acceptance decision.
What Lead Time Should You Expect From an HDI PCB Manufacturer in UK?
Published UK supplier examples place HDI prototypes from about 5 working days, while more complex HDI/BBV builds are commonly presented around 7–10 working days. Some suppliers advertise 1–5-day expedited options, but those are conditional services rather than a dependable default for every stackup.
Planning case
Indicative published range
What can extend it
Simple, materials-available HDI prototype
From about 5 working days
Open DFM questions, special material, via filling or added reports
More complex HDI or blind/buried-via build
About 7–10 working days as a planning reference
Multiple lamination cycles, stacked vias, tight registration or non-stock laminate
Expedited service
Some UK suppliers advertise 1–5 working days
Available only after design, material, capacity and inspection review
HDI plus assembly
Bare-board lead time plus component and PCBA schedule
Long-lead components, stencil, programming, X-ray or functional testing
The ranges are based on current supplier-published examples: Pure PCB lists HDI prototypes from five working days and an HDI/BBV range of 7–10 days, while Rush PCB UK advertises conditional 1–5-day quick-turn options. Treat them as RFQ planning references, not EBest promises or universal UK lead times. Ask the selected manufacturer to return a milestone schedule covering DFM approval, material release, lamination, drilling/filling, inspection, assembly and shipping.
How Should an HDI PCB Manufacturer in UK Select Materials?
An HDI PCB manufacturer in UK should select a material system from the electrical requirement, thermal exposure, lamination sequence, thickness target and supply risk—not from Tg alone.
For standard digital and industrial HDI: confirm that the chosen high-Tg FR-4 supports the required press cycles and finished thickness without uncontrolled material substitution.
For high-speed or RF nets: provide target Dk/Df assumptions, frequency and impedance geometry so the fabricator can model the actual construction.
For repeated reflow or higher thermal demand: review decomposition behavior, z-axis expansion and moisture control together with the assembly profile.
For thin dielectrics and microvias: verify that prepreg and core availability supports the required microvia depth, resin flow and copper distribution.
For procurement continuity: name the preferred grade and approved equivalent criteria; require notification before any change that affects impedance or lamination.
The RFQ should record manufacturer, grade, dielectric construction, copper type and weight, required electrical data, approved alternatives and substitution authority. The reviewed production stackup should be returned before release.
How Should an HDI PCB Manufacturer in UK Control Via-in-Pad?
An HDI PCB manufacturer in UK should control via-in-pad as a complete fill, cap and surface-planarity process. The buyer should verify:
Via geometry: define drill diameter, depth, aspect ratio and connected layers so the fill process is evaluated against the real structure.
Fill and cap: state whether conductive or non-conductive fill is required, the copper-cap expectation and any void acceptance criterion.
Planarity: specify the finished BGA/CSP pad requirement and inspection method because uneven pads can change paste volume and joint formation.
Surface finish: review finish selection and thickness after planarization; the final pad, not the unprocessed via, must meet assembly needs.
Fabrication-to-PCBA feedback: align stencil, reflow and X-ray inspection with pad acceptance so solder defects can be separated from bare-board defects.
Put these requirements in the fabrication drawing and via map. Do not rely on a note that says only “VIPPO” or “via-in-pad,” because it does not define the acceptance result.
How Should an HDI PCB Manufacturer in UK Plan Sequential Lamination?
An HDI PCB manufacturer in UK should translate the via map into a documented sequence of core preparation, lamination, laser drilling, filling and inspection.
Map every microvia span: show which vias are formed after each press cycle and where stacked interfaces occur.
Confirm the minimum necessary cycles: extra buildup stages increase alignment work, cost and lead time; remove a cycle when routing permits a simpler transition.
Control materials through repeated pressing: verify dielectric thickness, resin behavior and copper balance for the complete thermal history.
Protect registration: review capture pads, material movement allowances and the evidence used to verify interlayer alignment.
Define stage-specific inspection: identify which structures require microsection or other checks before later layers make them inaccessible.
Freeze the production stackup: require approval before changing layer sequence, material, site or via structure after prototype acceptance.
What Files Should You Send to an HDI PCB Manufacturer in UK?
A useful quote needs enough released data to identify the actual process route. Send the same package to each supplier.
Gerber or ODB++: release the copper, mask, legend and profile geometry from one controlled revision.
NC drill and microvia map: distinguish mechanical, buried, blind and laser-drilled holes and show every start/stop layer.
Production stackup: define the buildup, dielectric thicknesses, copper weights, material grades and finished thickness.
Fabrication drawing: state finished-hole rules, via fill/cap, surface finish, tolerances and special acceptance notes.
Quantity schedule: separate prototype, pilot and repeat volumes so tooling, panelization and unit pricing can be compared.
PCBA data when required: include BOM, pick-and-place, assembly drawing, approved substitutions and component-sourcing scope.
Inspection and test requirements: define electrical test, microsection, impedance, X-ray, programming and functional-test deliverables as applicable.
Commercial inputs: provide delivery destination, required date, Incoterm request and any country-of-manufacture restriction.
Also state prototype and repeat quantities, destination, origin constraints and required records. Ask for a reviewed stackup, deviations, proposed site and included inspection scope.
Submit the complete package with the RFQ and request an HDI DFM review covering both fabrication and assembly requirements.
How Should HDI PCB Manufacturers in UK Prevent Common Defects?
Prevent the main HDI defects by controlling the design input, process window and inspection point for each risk:
Microvia interconnect failure: keep the via diameter, depth and aspect ratio inside the approved process window; control laser drilling, interface preparation and plating; verify critical structures by electrical test and targeted microsection.
Incomplete via fill: match copper or resin fill to the via geometry, define acceptable voiding and inspect the filled structure before later processing hides it.
Poor via-in-pad planarity: specify fill, cap-plating and finished-pad requirements; inspect the surface before assembly to prevent solder wicking and inconsistent joints.
Layer misregistration: provide adequate capture pads, account for material movement and check alignment after each relevant lamination stage rather than only at final inspection.
Delamination: use a compatible material system, control moisture and contamination, and validate the press and thermal history for repeated lamination and reflow.
Impedance deviation: freeze dielectric thickness, copper geometry and material data in the production stackup; measure agreed coupons against the stated tolerance.
Open or short circuits: run 100% electrical testing against the correct released netlist and keep repair or concession records tied to the lot.
Prototype-to-volume drift: prevent unapproved changes to the factory, material, stackup, via treatment and inspection plan after the prototype is accepted.
FAQs About HDI PCB Manufacturers in UK
Q1: Are HDI PCBs always more expensive than standard multilayer PCBs?
A1: They usually involve additional processes, but the difference depends on buildup, microvias, materials, testing and quantity.
Q2: What is the minimum layer count for an HDI PCB?
A2: Layer count alone does not define HDI; high-density interconnection methods do.
Q3: Are stacked microvias better than staggered microvias?
A3: Neither is universally better. Select the structure from routing need and manufacturing risk.
Q4: Can HDI PCBs use controlled impedance?
A4: Yes. Provide target, tolerance, geometry and material assumptions and agree on coupon reporting.
Q5: Which surface finish suits fine-pitch HDI assembly?
A5: Choose it from pad geometry, assembly, storage and reliability needs, then review planarity with the assembler.
Q6: Do all microvias need to be filled?
A6: No. Filling depends on structure and use; via-in-pad and some stacked configurations need a defined fill and cap.
Q7: Should prototype and volume boards use the same stackup?
A7: The prototype should represent production where possible; later changes may require review or requalification.
Q8: Is DFM review necessary before production?
A8: Yes. It can find conflicting via structures, unsupported rules and incomplete acceptance criteria.
Q9: Can HDI boards use fine-pitch BGA and CSP packages?
A9: Yes, when pads, via treatment, finish, stencil, reflow and inspection are coordinated.
Q10: How should UK and overseas suppliers be compared?
A10: Use identical files, quantities, evidence, assembly scope, destination and change controls, then compare total responsibility and risk.
Conclusion
The right supplier turns a released HDI design into a controlled, inspectable and repeatable manufacturing plan. Confirm the build site, match capabilities to the stackup, require project-specific evidence and compare quotes on identical assumptions. Whether the route is UK in-house, UK-managed or overseas, technical ownership must remain clear from DFM through repeat production.
For an EBest quotation, send Gerber or ODB++, drill files, stackup, microvia map, fabrication drawing, impedance requirements, quantities, BOM, assembly data and test scope to sales@bestpcbs.com.
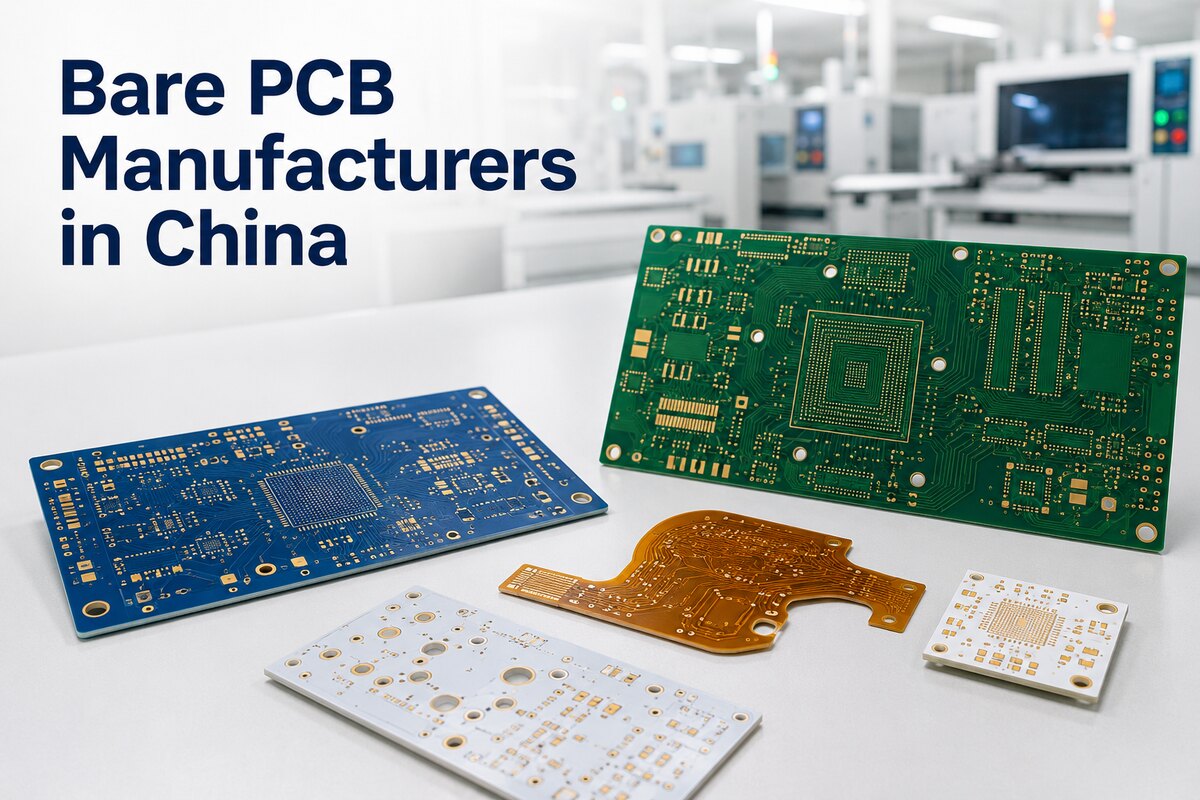
At EBest Circuit, we know that choosing among bare PCB board manufacturers in China requires more than comparing unit prices. We review technology fit, order volume, reliability class, documentation requirements, and delivery risk because a low quotation has little value if the approved construction cannot be reproduced consistently.
In this guide, we compare 10 established bare PCB manufacturers and explain how engineering and procurement teams can evaluate a bare PCB supplier. We also cover the bare PCB manufacturing process, materials, testing, defects, costs, and quotation files so that each supplier can be checked against the same requirements.
What Is a Bare PCB Board?
A bare printed circuit board is a fabricated circuit board without electronic components. It contains the conductive patterns, dielectric layers, plated holes, solder mask, surface finish, and identification markings needed for later assembly.
Depending on the design, a bare PCB may be:
Single-sided or double-sided
Multilayer rigid
HDI with blind, buried, or laser-drilled microvias
Flexible or rigid-flex
Metal-core or insulated metal substrate
Ceramic
Heavy copper
High-frequency or high-speed
Controlled-impedance
Bare-board manufacturing ends before component placement. PCB assembly adds solder paste, components, reflow or wave soldering, inspection, and functional testing.
Why Source Bare PCB Boards from China?
China has a broad PCB manufacturing base covering inexpensive standard FR-4 boards, rapid prototypes, high-volume automotive boards, HDI, rigid-flex, RF laminates, metal-core boards, and ceramic substrates. This range lets buyers choose a factory around the actual technology instead of forcing every project into one production model.
The main sourcing advantages are:
Access to multiple laminate and surface-finish options
Competitive prototype and volume pricing
Established component and electronics supply chains
Flexible tooling and panelization support
Engineering communication for custom stackups
Scalable production for growing programs
Export experience for North America, Europe, and other markets
The limitations are equally important. Long-distance communication, freight, customs clearance, engineering-change control, and intellectual-property protection must be managed deliberately. The purchase order should define materials, revision level, acceptance criteria, test requirements, packaging, and approved substitutions.
Top 10 Bare PCB Board Manufacturers in China
We prepared this buyer-oriented shortlist to show how different supplier models fit different projects. It is not an audited revenue ranking. We compare public manufacturing focus, likely project fit, and the level of engineering support that a buyer should confirm before production.
Manufacturer
Suitable project profile
Publicly stated product focus
EBest Circuit
Custom prototypes and mixed-technology projects
FR-4, metal-core, ceramic, HDI, heavy copper, RF, flex and rigid-flex
Shennan Circuits
High-reliability and high-complexity programs
PCB, package substrates and electronic assembly
Kinwong
Automotive, industrial and diversified volume production
Rigid, flex, rigid-flex, HDI, high-layer-count and metal-base PCB
Victory Giant Technology
AI computing, servers and advanced HDI
High-layer-count multilayer PCB, HDI, FPC and rigid-flex
Suntak Technology
Communications, automotive and industrial programs
Multilayer, HDI, high-speed, heavy-copper and special PCB
Avary Holding
High-volume compact electronics
FPC, SLP, HDI, rigid and rigid-flex PCB
Fastprint Circuit Tech
High-complexity development and specialized PCB
High-end PCB, FPC, IC substrates and semiconductor test boards
Bomin Electronics
Broad special-board requirements
HDI, microwave, heavy copper, metal-core, flex and rigid-flex
China Eagle Electronic
Flex, rigid-flex and automotive interconnects
Rigid PCB, FPC, rigid-flex and FPCA
Aoshikang Technology
Rigid PCB for servers, automotive and communications
Multilayer, HDI and application-specific rigid PCB
1. EBest Circuit
EBest Circuit was established in 2006, and we provide PCB fabrication and PCBA services from Shenzhen for international engineering and procurement teams. Our documented management systems and compliance credentials include ISO 9001:2015, ISO 13485:2016, IATF 16949, AS9100D, UL recognition E502832, RoHS, and REACH. The exact certificate scope and manufacturing-site applicability should still be confirmed for each regulated program.
We manufacture standard and multilayer FR-4, metal-core, ceramic, heavy-copper, HDI, RF, high-Tg, impedance-controlled, flexible, and rigid-flex boards. More importantly, we connect DFM and stack-up review, prototype validation, repeat production, component sourcing, and turnkey assembly through one technical communication path.
Qualification evidence: Our documented systems span general quality, medical-device, automotive, aerospace, product-safety, and environmental-compliance needs, subject to project and certificate scope.
Process-level inspection: We can define AOI, flying-probe or fixture electrical testing, impedance testing, microsection inspection, copper-thickness measurement, and final visual inspection according to the project.
Beyond fixed online menus: We can evaluate custom stack-ups, specified laminates, impedance requirements, special via structures, copper weights, and inspection needs before material release.
Prototype-to-volume continuity: We support prototype review, controlled pilot builds, and production transfer without treating engineering clarification as a separate service.
Multiple PCB technologies: Customers can discuss FR-4, HDI, RF, heavy-copper, metal-core, ceramic, flex, and rigid-flex requirements with the same team.
Bare PCB plus PCBA: When required, we can continue from bare board fabrication into component sourcing, assembly, inspection, and project-specific testing.
Corrective-action support: When a quality complaint requires formal investigation, our process can include problem classification, root-cause analysis, an 8D report, corrective action, and closure communication.
To compare our manufacturing route with the other suppliers in this list, send your Gerber or ODB++ data, fabrication drawing, stack-up, quantity, material, impedance, surface-finish, panelization, and test requirements to sales@bestpcbs.com. We will review the package and identify manufacturability, documentation, or cost risks before production.
2. Shennan Circuits
Shennan Circuits operates in printed circuit boards, package substrates, and electronic assembly. Its public profile emphasizes communications, medical equipment, and advanced electronic interconnection.
SCC is more relevant to qualified, technically demanding programs than to buyers seeking only the lowest prototype price. Prospective customers should discuss technology qualification, production-volume expectations, documentation, and onboarding requirements early.
3. Kinwong Electronic
Kinwong offers a wide technology range that includes high-layer-count boards, HDI, rigid-flex, metal-base PCB, and advanced interconnect structures. Its application coverage includes automotive electronics, industrial equipment, communications, computing, and consumer products.
It is well suited to buyers with sustained production demand and formal supplier-qualification processes. Confirm which production site will manufacture the board, because capability, certification scope, and approved materials can vary by facility.
4. Victory Giant Technology
Victory Giant Technology focuses on high-precision multilayer boards and advanced HDI. Its published product areas include AI and high-performance computing, automotive electronics, telecommunications, smart devices, industrial control, and medical equipment.
The company is a strong candidate for high-layer-count and high-speed platforms. Buyers should provide stackup constraints, loss targets, copper-foil requirements, impedance tables, back-drill details, and coupon requirements before requesting a firm production quotation.
5. Suntak Technology
Suntak Technology operates multiple PCB plants serving communications, data centers, automotive electronics, industrial control, computers, and medical equipment. Its published capabilities include multilayer, HDI, high-frequency, high-speed, heavy-copper, and other specialized constructions.
Suntak may suit medium-to-high-volume programs requiring established process control. Buyers should identify the intended factory and confirm that the relevant quality-system certification covers that manufacturing location.
6. Avary Holding
Avary Holding produces FPC, substrate-like PCB, HDI, rigid PCB, and rigid-flex products. Its strongest fit is generally compact, high-density electronics used in communications, consumer devices, computers, automotive systems, and servers.
Avary’s production profile is oriented toward substantial programs and demanding customer qualification. Smaller buyers should confirm minimum commercial expectations, engineering-access arrangements, tooling ownership, and forecast commitments before beginning qualification.
7. Fastprint Circuit Tech
Fastprint Circuit Tech works across high-end PCB, flexible circuits, IC package substrates, and semiconductor test boards. Its published application coverage includes communications, industrial control, rail transportation, medical electronics, computing, and automotive electronics.
It is worth evaluating for complex prototypes, high-mix engineering builds, and projects where design simulation or specialized interconnect experience is required. Confirm whether the quoted service is prototype-focused or intended for repeat volume production.
8. Bomin Electronics
Bomin Electronics manufactures HDI, high-layer-count, microwave and high-frequency, heavy-copper, metal-core, flexible, rigid-flex, and ceramic products. Its factories serve communications, medical, aerospace, industrial, computing, automotive, and energy applications.
This range makes Bomin relevant when a purchasing team wants to consolidate several board technologies. Qualification should still be performed by product family because a factory experienced in HDI is not automatically the best source for ceramic or metal-core boards.
9. China Eagle Electronic Technology
China Eagle Electronic Technology provides rigid PCB, flexible PCB, rigid-flex PCB, and flexible circuit assembly. Its product mix is relevant to automotive electronics, smart devices, medical products, and applications where flexible interconnects replace connectors or wire harnesses.
Buyers should review bend-area construction, coverlay openings, stiffeners, adhesive systems, dimensional tolerances, and dynamic-flex requirements. Flex and rigid-flex projects need more application information than a conventional rigid-board quotation.
10. Aoshikang Technology
Aoshikang Technology focuses on PCB products for automotive electronics, data storage and servers, communications, consumer electronics, and digital-energy applications. It is primarily a candidate for rigid multilayer and production-oriented programs.
Before selection, buyers should confirm current line-and-space capability, via structures, high-speed material availability, surface finishes, approved production site, and the commercial fit for the forecast volume.
Which Bare PCB Types Can Chinese Manufacturers Produce?
Not every supplier should be asked to build every PCB type. A factory’s best-fit technology usually reflects its equipment, material system, process history, and customer base.
Standard FR-4 PCB: Suitable for consumer, industrial, control, and general electronic products.
High-Tg PCB: Used when assembly temperatures, operating temperatures, or layer count demand greater thermal resistance.
HDI PCB: Provides higher routing density through laser microvias, sequential lamination, via-in-pad, and fine features.
High-speed PCB: Uses controlled stackups, low-loss materials, smooth copper, impedance control, and loss verification where required.
RF and microwave PCB: Built with materials such as Rogers, Taconic, or other specified RF laminates.
Heavy-copper PCB: Supports higher current and stronger thermal conduction but requires greater spacing and specialized etching.
Metal-core PCB: Transfers heat from LEDs and power devices through an insulated aluminum or copper base.
Flex and rigid-flex PCB: Reduces interconnect size and weight but introduces bend-radius, coverlay, and dimensional-control requirements.
Ceramic PCB: Used for thermal, high-frequency, high-voltage, or hermetic applications where FR-4 is unsuitable.
A broad capability list is not proof of equal competence in every category. Ask for a capability statement, representative build, stackup review, and applicable qualification evidence for the specific technology.
Which PCB Materials and Surface Finishes Are Available?
PCB material selection must follow the electrical, thermal, mechanical, and assembly requirements. “FR-4” alone is not a complete specification because resin systems differ in Tg, decomposition temperature, loss, expansion, and CAF resistance.
Requirement
Typical material or finish
Main purchasing concern
General industrial PCB
Standard or high-Tg FR-4
Approved laminate brand and Tg
High-speed digital
Low-loss or ultra-low-loss laminate
Dk, Df, copper roughness and availability
RF and microwave
Hydrocarbon-ceramic or PTFE-based laminate
RF grade, thickness and mixed-material processing
High current
Heavy copper FR-4
Finished copper tolerance and conductor spacing
LED or power conversion
Aluminum- or copper-base material
Dielectric thermal performance and isolation
Flexible circuits
Polyimide with adhesive or adhesiveless copper
Bend life, coverlay and dimensional stability
Fine-pitch assembly
ENIG, ENEPIG or immersion silver
Pad flatness, storage and assembly compatibility
Cost-sensitive soldering
Lead-free HASL
Surface flatness and thermal exposure
Press-fit or contact edge
Selective gold or hard gold
Nickel/gold thickness and contact-area definition
Do not permit an unapproved laminate substitution based only on a supplier’s claim that two materials are “equivalent.” The substitution review should compare dielectric properties, thermal behavior, copper type, thickness tolerance, flammability status, and qualification history.
How Does the Bare PCB Manufacturing Process Work?
The process begins with engineering review rather than drilling or imaging. CAM engineers inspect the fabrication files, netlist, stackup, drill data, tolerances, panelization, and special requirements before releasing production data.
A typical multilayer process includes:
Incoming laminate and copper-foil inspection
Inner-layer imaging and etching
Automated optical inspection of inner circuitry
Oxide or oxide-alternative surface preparation
Layup and multilayer lamination
Mechanical or laser drilling
Desmear and hole-wall preparation
Electroless copper and electrolytic plating
Outer-layer imaging and pattern plating
Final etching
Solder-mask application
Surface finishing
Profiling, routing, V-scoring, or laser cutting
Electrical testing
Visual and dimensional inspection
Cleaning, packaging, and shipment
HDI, rigid-flex, RF, heavy-copper, metal-core, and ceramic boards require modified process flows. The manufacturer should describe the actual production route when it affects reliability, lead time, or cost.
Which Tests and Quality Standards Matter?
A certificate does not replace product-specific inspection. Buyers should define the acceptance class, inspection plan, electrical-test coverage, and required reports on the purchase order. See our PCB testing guide for a broader comparison of test methods and acceptance goals.
Commonly referenced requirements include:
IPC-6012 for qualification and performance of rigid printed boards
IPC-6013 for flexible and rigid-flex boards
IPC-A-600 for visual acceptability of printed boards
IPC-9252B for electrical testing of unpopulated boards
ISO 9001 for general quality-management systems
IATF 16949 for applicable automotive supply chains
ISO 13485 for medical-device quality systems
AS9100 for aerospace quality-management systems
UL recognition where the end product or customer specification requires it
RoHS or REACH declarations for applicable markets and materials
The following comparison summarizes certifications and management systems publicly listed by the manufacturers or in EBest Circuit’s verified company records as of August 25, 2026. It is a qualification starting point, not proof that every certificate covers every factory, product, or current order.
Manufacturer
Publicly listed certifications or systems
EBest Circuit
ISO 9001:2015; ISO 13485:2016; IATF 16949; AS9100D; UL E502832; RoHS; REACH
Shennan Circuits
ISO 9001; IATF 16949; AS9100; Nadcap; ISO 13485
Kinwong Electronic
ISO 9001; IATF 16949; ISO 13485; ISO/IEC 17025; ISO 14001; ISO/IEC 27001; QC 080000
Victory Giant Technology
UL; ISO 9001; ISO 14001; ISO 45001; IATF 16949; CQC; QC 080000; China RoHS
Suntak Technology
ISO 9001; IATF 16949; AS9100; ISO 13485; ISO 14001; ISO 45001; ISO 27001; QC 080000
Avary Holding
ISO 9001; IATF 16949; QC 080000; ISO 14001; ISO 45001; ISO 50001; UL; CQC
Fastprint Circuit Tech
ISO 9001; IATF 16949; ISO 13485; ESD S20.20; UL; RoHS; REACH
Bomin Electronics
ISO 9001; IATF 16949; ISO 13485; AS9100D; ISO 14001; ISO 45001; QC 080000; UL
China Eagle Electronic Technology
ISO 9001; IATF 16949; ISO 14001; ISO 45001; ISO/IEC 27001; QC 080000
Aoshikang Technology
ISO 9001; IATF 16949; ISO 13485; ISO 14001; ISO 27001; CQC; SA8000
Before supplier approval, request the current certificate PDF and verify the legal entity, manufacturing address, certified activity, issue and expiry dates, and whether the quoted production site is inside the scope.
The quality plan may include AOI, flying-probe or fixture electrical testing, impedance coupons, microsections, plating-thickness measurements, ionic-contamination testing, solderability testing, thermal stress, dimensional inspection, and final visual inspection.
Certification must be checked by legal entity, manufacturing address, scope, and expiry date. A sales office’s certificate does not automatically cover a separate factory.
What Common Bare PCB Defects Should Buyers Watch For?
Most recurring defects can be traced to incomplete data, an unstable process, or requirements that were never defined.
Defect
Likely cause
Prevention or verification
Open or short circuit
Imaging, etching, contamination, or plating defect
Netlist-based electrical test and AOI
Thin hole-wall copper
Poor activation or plating distribution
Microsection and copper-thickness report
Delamination
Moisture, weak bonding, or unsuitable lamination
Material control, thermal stress and microsection
Impedance deviation
Wrong stackup, Dk assumption, trace geometry, or copper thickness
Approved stackup, coupon and TDR test
Solder-mask misregistration
Imaging or dimensional compensation error
Defined mask clearance and visual inspection
Pad lifting
Excessive thermal stress or weak copper adhesion
Material review and assembly-profile validation
Surface-finish defects
Poor process control, contamination, or excessive storage
Finish-thickness test, solderability check and sealed packaging
Warpage
Unbalanced copper, asymmetric stackup, or thermal stress
Balanced construction and flatness inspection
CAF or leakage risk
Moisture, contamination, small spacing, or material weakness
Material selection, cleanliness control and reliability testing
A “100% electrical test” detects opens and shorts, but it does not prove correct dielectric thickness, plating quality, solder-mask registration, surface finish, or long-term thermal reliability.
What Determines Bare PCB Cost in China?
PCB pricing is driven by manufacturing difficulty and panel utilization, not simply board area. The largest cost changes usually come from material choice, layer count, via technology, tolerances, and order volume.
Major cost factors include:
Board dimensions and array layout
Layer count and finished thickness
Standard versus low-loss or RF materials
Copper weight and plated-hole requirements
Minimum trace width and spacing
Mechanical holes, blind vias, buried vias, and microvias
Sequential lamination cycles
Controlled impedance and test coupons
Surface finish and selective plating
Routing, V-scoring, countersinks, cavities, and edge plating
Inspection reports and reliability testing
Prototype quantity, production volume, and delivery schedule
Freight, insurance, duties, and payment terms
The lowest unit price may use a different laminate, copper construction, test method, or delivery term. Compare quotations against one controlled specification and calculate landed cost rather than comparing only the factory price.
Which Industries Use Bare PCBs Manufactured in China?
Chinese PCB manufacturers supply boards for products ranging from simple controls to high-reliability electronics. The application determines the process controls and documents that matter.
Automotive: ECUs, battery-management systems, lighting, radar, infotainment, charging, and power conversion
Industrial: PLCs, motor drives, sensors, robotics, instrumentation, and power supplies
Communications: Base stations, routers, switches, optical modules, antennas, and microwave equipment
Medical: Monitoring, diagnostic, imaging, laboratory, and portable medical devices
Aerospace: Avionics, control, sensing, communication, and test equipment
Energy: Solar inverters, energy storage, charging systems, smart meters, and industrial power conversion
Consumer electronics: Smart-home devices, wearables, displays, appliances, and portable products
LED lighting: Automotive lamps, industrial lighting, outdoor displays, and high-power LED modules
A board intended for an industrial controller should not automatically be purchased under automotive or aerospace controls. Higher assurance levels increase documentation, testing, material traceability, and cost, so they should be specified only when the product requires them.
How Should Buyers Evaluate a Chinese Bare PCB Supplier?
Start with technology fit, then evaluate process control and commercial reliability. A polished website or low sample price does not establish production capability.
Ask each candidate to confirm:
Which factory will manufacture the PCB
Whether critical processes are performed internally or outsourced
Experience with the specified materials and via structures
Minimum production rules and preferred design rules
Quality-system certificates covering that site
Material and production-lot traceability
Electrical-test and inspection methods
Engineering-change and deviation-approval procedures
Prototype-to-production transfer controls
Capacity for forecast demand
Complaint response and corrective-action process
Packaging, Incoterms, freight, and customs documentation
Ownership and protection of design files and tooling
For a high-risk program, begin with a technical audit or pilot order. Review cross-sections, impedance results, material certificates, dimensional reports, and corrective-action quality before approving volume production.
How Can Overseas Buyers Reduce Sourcing Risk?
The most effective protection is a complete technical agreement that follows the board through quotation, fabrication, inspection, and shipment.
For North American and European orders:
Define the governing IPC specification and acceptance class.
Request certificates only when they apply to the product and manufacturing site.
State whether RoHS, REACH, UL materials, conflict-mineral reporting, or other declarations are required.
Confirm Incoterms and responsibility for freight, insurance, duties, and customs clearance.
Require approval before changing laminate brands, copper foil, solder mask, surface finish, or manufacturing location.
Use revision-controlled Gerber or ODB++, drill, netlist, drawing, and stackup files.
Approve a pilot lot before transferring a high-reliability design to volume production.
Keep an approved sample and inspection records for future lot comparison.
China-based manufacturing does not require a supplier to claim a foreign factory or warehouse. Reliable global supply depends on clear export documentation, realistic logistics planning, and responsive engineering communication.
What Files Are Needed for a Bare PCB Quote?
A complete RFQ reduces assumptions and makes supplier quotations easier to compare.
Provide:
Gerber X2, ODB++, IPC-2581, or other agreed fabrication data
NC drill and route files
Readme or fabrication drawing
Layer count and proposed stackup
Board dimensions and panel requirements
Base and finished copper weights
Laminate manufacturer and material grade
Finished thickness and tolerances
Minimum trace width and spacing
Minimum finished-hole size
Via types and filling or capping requirements
Controlled-impedance table
Surface finish
Solder-mask and legend requirements
Acceptance class and electrical-test requirements
Special mechanical features
Prototype and annual quantities
Target delivery date and shipping destination
Required certificates and inspection reports
If the stackup is not finalized, provide impedance targets, frequency range, loss constraints, thickness limits, and preferred materials. The manufacturer can then propose a producible stackup for approval.
At EBest Circuit, we review these files before production and support custom stack-ups, prototypes, volume bare-board manufacturing, and optional assembly. Complete RFQ data lets our engineers identify cost, material, documentation, and manufacturability risks while changes are still inexpensive.
Why Choose EBest Circuit as Your China Bare Board PCB Manufacturer?
The manufacturers above serve different market segments. At EBest Circuit, our differentiator is the combination of special-board experience, direct engineering review, and a practical path from prototype to repeat production and optional PCBA. We are a strong fit when the project cannot be reduced to a fixed standard-order menu.
We support customers in several practical areas:
Early DFM and stack-up review before material release
Custom laminate, copper, via, impedance, surface-finish, and inspection evaluation
Standard FR-4 and specialized HDI, RF, heavy-copper, metal-core, ceramic, flex, and rigid-flex options
Prototype validation followed by controlled production transfer
Material and production-lot traceability based on project requirements
Bare PCB fabrication with optional component sourcing, PCB assembly, inspection, and testing
One technical communication path from quotation through production
Export support for global customers without claiming unverified overseas factories or warehouses
Our quality management systems follow ISO 9001, ISO 13485, IATF 16949, and AS9100D requirements, helping us maintain strict quality control throughout every stage of manufacturing. The applicable certification, manufacturing location, inspection plan, and acceptance class should be confirmed for each project rather than assumed from the board type alone.
For technical review and quotation, send your Gerber files or PCB requirements to sales@bestpcbs.com. Our engineering team will review the construction, return the key manufacturing questions, and identify cost or reliability risks before production.
FAQs About Bare PCB Board Manufacturers in China
What is the difference between a bare PCB manufacturer and a PCBA manufacturer?
A bare PCB manufacturer fabricates the board structure, including copper circuits, vias, solder mask, surface finish, and profile. A PCBA manufacturer installs and solders electronic components. Some Chinese suppliers provide both services, but buyers should evaluate bare-board fabrication and assembly capabilities separately.
How do I verify that a Chinese PCB supplier is a real manufacturer?
Request the factory’s registered legal name, physical production address, business license, capability statement, equipment list, and site-specific certificates. A video audit, third-party audit, or onsite visit can confirm production activity. Also ask which processes are outsourced and which facility will build your order.
What is a reasonable minimum order quantity for bare PCBs?
MOQ depends on the production model. Prototype factories may accept a few boards, while large-volume manufacturers may require higher commercial commitments. The relevant question is whether the same material, process route, test method, and factory can support both the prototype and expected production volume.
Can Chinese manufacturers build IPC Class 3 bare PCBs?
Some can, but IPC Class 3 should be stated on the drawing and purchase order rather than assumed from a sales claim. Confirm the applicable IPC performance specification, inspection criteria, testing, documentation, coupon design, and acceptance agreement before production. Request supporting reports for the pilot lot.
Should I choose ENIG or lead-free HASL for a bare PCB?
Lead-free HASL is economical but less flat, which can be problematic for fine-pitch components. ENIG provides a flatter surface and is commonly used for BGA, QFN, and fine-pitch assembly. The correct choice depends on pad geometry, storage time, assembly process, contact function, and budget.
Can a prototype PCB be transferred directly to mass production?
Only if the construction and process are controlled. Before transfer, freeze the stackup, material grade, copper foil, drill structure, surface finish, test requirements, and approved production files. If a different factory or panel format will be used, request a new engineering review and pilot lot. For related planning, see our prototype PCB guide.
What quality documents should I request with a PCB shipment?
The required package may include a certificate of conformance, electrical-test confirmation, material certificate, impedance report, microsection report, dimensional inspection, plating measurements, solderability results, and lot traceability. Request only documents that support actual product risks, and define them before quotation.
Choosing among bare PCB board manufacturers in China starts with a controlled specification and an honest assessment of project risk. Standard FR-4 prototypes, automotive multilayers, server backplanes, HDI, RF, heavy-copper, flex, and ceramic boards require different factories and qualification methods. Approve the stackup, materials, test plan, production site, and pilot results before committing to volume. Use this bare pcb board manufacturers in China comparison as a supplier-qualification reference.
If you need OEM manufacturing, prototype development, volume bare-board production, or a custom PCB and PCBA solution, send your project files to our engineering team at sales@bestpcbs.com for technical review and a quotation.
High speed PCB design is the discipline of controlling how fast signal edges travel through a real interconnect. A successful board needs more than clean routing: the stackup, dielectric system, trace geometry, reference planes, vias, connectors, power distribution network, and fabrication tolerances must work as one electrical structure.
This guide explains the decisions that should be settled before routing, the checks that protect signal and power integrity, and the manufacturing information a PCB supplier needs. The goal is not to promote one universal spacing or length rule. It is to show how interface requirements become a controlled, testable board construction.
What Is High Speed PCB Design?
High speed PCB design begins when an interconnect can no longer be treated as an ideal wire. During a fast transition, the trace, return plane, vias, pads, connectors, and package behave as a transmission path with distributed inductance, capacitance, resistance, and dielectric loss.
The important design questions are therefore electrical and physical at the same time:
Will the channel maintain the required characteristic impedance?
Can return current follow the signal without crossing a plane split or large discontinuity?
Are insertion loss, reflection, crosstalk, jitter, and skew within the interface budget?
Can the selected material, stackup, via structure, and trace geometry be manufactured repeatedly?
How will the finished board be tested against the released requirements?
When Does a PCB Signal Become High Speed?
A signal becomes a high-speed layout problem when its transition time is short enough for the physical interconnect delay to matter. Clock frequency alone is not a reliable boundary. A moderate-frequency clock with a sharp edge may require transmission-line treatment, while a higher-frequency but slower edge on a short connection may be less demanding.
Start with the driver rise and fall times, not only the advertised data rate. Compare the edge time with the propagation delay of the complete path, including packages, traces, vias, connectors, and cables. When the signal can encounter a meaningful impedance change before the transition has settled, reflection and return-path control become design constraints.
Evidence
What It Changes
Fast edge relative to channel delay
Treat the route as a transmission line
Long channel or high data rate
Evaluate insertion loss and equalization margin
Parallel high-speed buses
Control timing, skew, coupling, and reference planes
Dense BGA escape
Plan layer transitions, via geometry, and return vias early
Low-voltage high-current ICs
Design the PDN against a target-impedance requirement
High Speed PCB Design Guidelines
The most reliable high speed PCB design guidelines form a sequence: classify interfaces, plan placement, freeze the stackup with the fabricator, define impedance and timing constraints, route the most critical nets first, simulate where margin is uncertain, and verify the released fabrication data.
Classify signal groups. Record interface standard, data rate, edge rate, target impedance, topology, timing limits, and expected channel length.
Place around signal flow. Keep high-speed paths short and direct while reserving space for termination, decoupling, escape routing, and test access.
Agree on a manufacturable stackup. Confirm laminate family, dielectric thickness, copper weight, layer order, finished board thickness, and impedance structures before final routing.
Protect return paths. Route each critical signal over a continuous reference plane and provide a local return transition when the signal changes reference layers.
Control discontinuities. Review connector launches, pads, neck-down sections, vias, stubs, test points, and plane voids as part of the channel.
Verify, do not guess. Use the interface vendor’s layout guide, field-solver results, SI/PI simulation, DRC constraints, and fabrication feedback.
These high speed PCB design rules are a framework, not a substitute for the component manufacturer’s limits. A generic rule should never override a tighter PCIe, DDR, USB, Ethernet, HDMI, MIPI, SerDes, or FPGA requirement.
How Should the PCB Stackup Be Planned?
The stackup should be planned before detailed routing because it determines the available reference planes, impedance geometry, layer-transition behavior, dielectric loss, copper roughness exposure, and routing capacity. Changing it after routing can invalidate trace widths, differential spacing, propagation delay, and loss estimates.
Each critical signal layer should have a nearby continuous reference plane. Avoid placing two high-speed signal layers next to each other without a plane between them unless coupling has been evaluated. Power and ground planes placed close together can also improve high-frequency plane capacitance, but the PDN still needs a complete impedance analysis.
Do not select layer count from a generic chart alone. I/O density, escape routing, number of high-speed interfaces, power rails, board thickness, via structures, shielding needs, and cost all influence the construction. Before routing, ask the fabricator to confirm that the proposed dielectric thicknesses, copper weights, materials, and trace geometries are available and controllable.
Which Materials Work for High Speed PCB Design?
The right material is the lowest-cost system that still meets the channel’s loss, impedance, thermal, reliability, and fabrication requirements. Standard FR-4 can support many short, moderate-speed channels, while longer routes and higher Nyquist frequencies may require lower-loss laminates.
Material Decision
Engineering Impact
Dk and its tolerance
Affects impedance and propagation delay
Df at the relevant frequency
Contributes to dielectric insertion loss
Copper roughness
Increases conductor loss as frequency rises
Glass-weave construction
Can influence differential skew in sensitive channels
Resin system and Tg
Affect fabrication, thermal reliability, and lead-free processing
Material availability
Changes achievable stackup, cost, and production continuity
Material data must be evaluated at the frequency and test method relevant to the design. Marketing labels such as “high speed” or “low loss” do not by themselves prove that a laminate meets the channel budget. Hybrid constructions can reduce cost, but bonding, z-axis expansion, copper treatment, drill behavior, and stackup symmetry still need fabrication review.
How Do Controlled Impedance and Return Paths Work?
Controlled impedance depends on the complete transmission-line geometry: trace width and thickness, dielectric height, Dk, nearby copper, reference-plane continuity, and differential-pair spacing. The target comes from the interface specification; the final trace geometry should come from the released stackup and an appropriate field solver.
A continuous return path is equally important. High-frequency return current concentrates near the signal route on its reference plane. If the trace crosses a split, void, anti-pad field, connector discontinuity, or poorly planned reference-layer change, the current must detour. That larger loop increases inductance, radiation, coupling, and impedance disturbance.
For a deeper manufacturing view, see our impedance control PCB guide. The fabrication drawing should state the controlled nets, target values, tolerance, reference layer, coupon requirement, and any reporting requirement rather than relying on trace width alone.
What Are the Key Differential Pair and Length-Matching Rules?
Differential-pair routing should preserve the impedance, symmetry, return path, and timing budget defined by the interface. Pair spacing and length tolerance are not universal numbers; they depend on the stackup, coupling mode, data rate, receiver margin, and vendor specification.
Route both conductors on the same layer with consistent width and spacing where possible.
Keep reference-plane conditions and via transitions symmetrical.
Limit unnecessary uncoupled sections around pads, vias, and connectors.
Apply intra-pair and inter-lane tuning only to the groups that require it.
Avoid dense serpentine tuning that creates self-coupling or moves delay into an electrically different area.
Check skew in time, not only in physical length, when layers or materials differ.
Our differential pair PCB guide explains impedance, routing, and length matching in more detail. For final verification, inspect the complete channel rather than judging a pair only by its visual symmetry.
How Should Vias and Layer Transitions Be Managed?
Every high-speed via transition adds an impedance discontinuity and changes the return-current path. The effect depends on barrel length, pad and anti-pad geometry, unused stub length, layer assignment, nearby return vias, and the frequency content of the signal.
Keep the number of transitions as low as the routing allows. When a signal changes layers, provide a nearby ground return via if its reference plane changes. For demanding serial channels, model the launch and review whether backdrilling, blind vias, or HDI microvias are justified. These options can improve the channel, but they also change manufacturing cost, registration requirements, and inspection needs.
Read our PCB backdrill guide before specifying stub removal. The drawing should define the drilled-from side, target layer, residual stub requirement, applicable holes, and inspection method.
How Do Power Integrity and Decoupling Affect the Layout?
Power integrity affects timing margin because high-speed receivers and transmitters rely on stable supply rails and low-noise references. The PDN should remain below its target impedance across the frequency range where the voltage regulator, bulk capacitors, MLCCs, package, and plane structure supply transient current.
Place decoupling capacitors to minimize the current loop through the capacitor pads, vias, planes, and IC power pins. Select values and packages from an impedance model rather than assuming that more capacitance always solves the problem. Anti-resonance between components, via inductance, plane spreading inductance, and package effects can create unexpected peaks.
Our high-speed PCB power integrity guide covers PDN analysis and simulation. SI and PI reviews should share the same stackup because return planes, reference noise, and power-plane cavities can affect the observed eye.
Which High Speed PCB Design Software and Simulation Tools Are Useful?
High speed PCB design software should support constraint-driven routing, stackup and impedance definition, differential pairs, length and delay tuning, design-rule checking, and manufacturable output. Simulation tools are most valuable when they answer a specific risk question rather than producing plots without acceptance criteria.
Tool Function
Question It Should Answer
2D field solver
Which trace geometry meets the impedance target?
Pre-layout SI simulation
Which topology, termination, stackup, and material provide margin?
Post-layout channel simulation
Do routing, vias, connectors, and loss meet the eye or channel requirement?
PI/PDN simulation
Does the supply network stay below target impedance?
EMI/EMC analysis
Where do return discontinuities and resonant structures create risk?
Manufacturing DRC/DFM
Can the released geometry be fabricated and inspected consistently?
Use the component vendor’s IBIS or other approved models where available, and document assumptions such as material properties, copper roughness, package models, connector models, temperature, and process tolerance. A simulation is only as credible as its model boundaries.
What DFM Data Should Be Agreed With the Fabricator?
High-speed DFM should begin before final routing, not after Gerber export. The designer and PCB manufacturer must agree on the stackup and impedance construction because a small change in dielectric thickness, copper weight, material, or etching compensation can change the electrical result.
Released stackup with material family, core and prepreg selection, copper weights, and finished thickness
Controlled-impedance table with net class, target, tolerance, layer, and reference plane
Critical trace, pair, spacing, delay, and skew constraints
Via types, backdrill details, filled-via requirements, and residual-stub limits
Coupon design, impedance test method, report format, and acceptance criteria
Material substitution rules and the approval path for any stackup change
Gerber or ODB++ data, drill files, netlist, fabrication drawing, and revision control
These high speed PCB design considerations also affect quotation. Low-loss laminates, tighter impedance tolerance, additional layers, HDI structures, backdrilling, extra coupons, and specialized testing may improve performance but can increase material cost, process steps, and lead time.
What Common Failures Should Be Checked Before Fabrication?
The most expensive high-speed failures are often created before fabrication data is released. A focused review should look for discontinuities and requirement gaps that a normal connectivity DRC cannot detect.
Failure Risk
Pre-Fabrication Check
Reflection or poor eye opening
Review impedance changes, launches, stubs, termination, and channel loss
Crosstalk
Check parallel exposure, layer assignment, spacing, and reference-plane shielding
Unexpected skew
Compare electrical delay through layers, vias, packages, and fiber weave
EMI failure
Trace return-current paths and inspect splits, voids, connectors, and loop areas
PDN resonance
Review target impedance, capacitor models, mounting inductance, planes, and package
Fabrication mismatch
Freeze the approved stackup, material, impedance table, coupons, and substitution rules
Post-layout simulation and prototype measurements should target the interfaces with the least margin. Depending on the product, verification may include TDR, impedance coupons, VNA measurements, eye diagrams, jitter analysis, bit-error-rate testing, protocol compliance testing, and functional stress tests. Our eye diagram signal integrity guide explains how to interpret eye height, width, jitter, and closure.
FAQ About High Speed PCB Design
Is every high-frequency clock automatically a high-speed PCB signal?
No. The decision depends on edge time, channel delay, interconnect geometry, and required margin. A lower-frequency signal with a fast edge and long trace may need transmission-line treatment, while a physically short route with slower transitions may be less sensitive.
Can a four-layer PCB support high-speed interfaces?
It can support some interfaces when the stackup provides continuous references and sufficient routing space. The correct layer count depends on I/O density, power rails, interface count, loss targets, via strategy, and EMC requirements. Do not select four layers only because a generic example worked elsewhere.
Are 50-ohm and 100-ohm impedance values always required?
No. They are common targets, but the correct single-ended or differential impedance comes from the interface specification. Some standards use other values. The drawing and impedance table should state the exact target, tolerance, layer, reference plane, and controlled nets.
Does every high-speed PCB require a low-loss laminate?
No. Material selection depends on channel length, Nyquist frequency, insertion-loss budget, copper roughness, temperature, reliability, and cost. Shorter channels may work on suitable FR-4 systems, while longer or faster links may need lower-loss materials.
Should all differential pairs be length matched?
Match only to the tolerance required by the interface and timing budget. Unnecessary tuning can add loss, coupling, and routing congestion. The design should distinguish intra-pair skew, lane-to-lane skew, bus timing, and absolute maximum length.
What files help a PCB manufacturer review a high-speed design?
Provide Gerber or ODB++ data, drill files, netlist, fabrication drawing, released stackup, material requirements, impedance table, critical constraints, backdrill details, coupon requirements, quantity, and revision information. Share the substitution and approval rules before material procurement.
How Can EBest Circuit Support High Speed PCB Design and Manufacturing?
At EBest Circuit, we support a manufacturable high speed PCB design from stackup and DFM review through prototype fabrication, testing, repeat production, and optional PCB assembly. Our verified capabilities include high-speed PCB, high-frequency PCB, HDI, multilayer FR-4, impedance control, AOI, electrical testing, impedance testing, microsection inspection, and copper-thickness testing.
Send your Gerber or ODB++ data, stackup, impedance table, material preference, via and backdrill requirements, quantity, and test requirements to sales@bestpcbs.com. We will review the construction and identify questions that should be resolved before material release and production.
A heavy copper PCB manufacturer builds boards for applications that require higher current capacity, improved heat dissipation, and stronger mechanical reliability than standard copper PCB constructions. By increasing copper thickness on inner or outer layers, these PCBs can support high-power circuits used in battery systems, power converters, industrial equipment, EV charging systems, renewable energy controls, and other demanding electrical applications.
EBest Circuit provides custom heavy copper PCB manufacturing with support for thick copper layers, mixed copper stack-ups, high-current designs, and complex multilayer structures. Our engineering team reviews copper thickness, layer configuration, thermal requirements, via structures, and manufacturing feasibility before production to help customers develop reliable power PCB solutions. Send your Gerber files, stack-up requirements, or application details to sales@bestpcbs.com for engineering review and quotation.
What Maximum Copper Thickness Can Be Achieved for Heavy Copper PCBs?
The maximum copper thickness of a heavy copper PCB depends on the layer position, board size, copper distribution, etching requirements, and manufacturing process capability. Unlike standard PCBs using 1 oz or 2 oz copper, heavy copper designs require specialized processing to maintain copper thickness consistency and reliable circuit formation.
EBest Circuit supports the following verified standard and special-project copper ranges. PCB copper weight must be evaluated with board size, copper distribution, spacing, dielectric fill, and process requirements.
Copper Location
Typical Thickness Capability
Inner layer copper
Standard 0.5–5 oz; special projects 5–20 oz
Outer layer copper
Standard 1–5 oz; special projects 5–20 oz
Mixed copper designs
Available after stack-up and DFM review
100 oz+ request
Project-specific engineering review; not a standard capability
For 100 oz+ copper PCB designs, additional engineering evaluation is required because extremely thick copper affects:
Trace geometry and etching compensation
Copper distribution balance
Lamination pressure and resin filling
Thermal stress during manufacturing
Finished board weight and mechanical strength
Heavy copper capability is not only determined by copper thickness. A reliable manufacturing process must also maintain proper layer alignment, insulation spacing, and plated hole quality.
What Heavy Copper PCB Stack-Up Configurations Are Available?
Heavy copper PCBs can be manufactured with different stack-up structures depending on current requirements, thermal performance, signal requirements, and cost targets.
Typical configurations include:
Stack-Up Type
Typical Application
4-layer heavy copper PCB
Power control boards, industrial electronics
6-layer mixed copper PCB
Power and signal integration
Heavy copper outer layers with standard inner layers
High current connection areas
Heavy copper power layers with thermal vias
Heat-sensitive applications
A high current PCB stackup often combines heavy copper layers with standard signal layers. This approach allows engineers to increase current capacity in specific areas without unnecessarily increasing the cost and weight of the entire PCB.
A typical multilayer structure may include:
Thick copper power planes for current distribution
Standard copper signal layers for control circuits
Dedicated thermal layers for heat spreading
Controlled impedance layers when high-speed signals are required
The final stack-up should be reviewed during the engineering stage to ensure copper thickness, dielectric thickness, and manufacturing capability are properly matched.
Which Materials and Prepreg Systems Are Used for Heavy Copper PCBs?
Heavy copper PCB materials must provide sufficient mechanical strength, thermal stability, and reliable insulation performance under high current operation.
Common material options include:
Material System
Application Advantage
Standard FR-4
General heavy copper applications
High Tg FR-4
Higher thermal reliability
Thermal management materials
Improved heat dissipation
High resin content prepreg
Better copper gap filling
Prepreg selection is especially important for heavy copper multilayer boards. Thick copper creates larger height differences between copper areas, requiring sufficient resin flow during lamination to prevent voids and ensure reliable insulation.
Material selection depends on:
Operating temperature
Current load
Thermal cycling requirements
Mechanical environment
Industry requirements
For high-power applications, engineers should consider both copper thickness and laminate performance rather than focusing only on copper weight.
What Surface Finish Options Are Available for Heavy Copper PCBs?
Surface finish selection depends on component requirements, assembly process, reliability expectations, and storage conditions.
Common surface finishes for heavy copper PCBs include:
Surface Finish
Typical Application
ENIG
Fine-pitch components and high reliability applications
Lead-free HASL
Cost-effective industrial applications
HASL
Traditional soldering applications
OSP
Short-term storage and standard assembly
For high-current PCBs, surface finish selection should also consider:
Contact reliability
Solder joint performance
Assembly temperature profile
Long-term environmental exposure
The correct surface finish helps maintain reliable electrical connections throughout the product lifecycle.
What Are the Design Rules and Manufacturing Tolerances for Heavy Copper PCBs?
Heavy copper PCB design requires additional attention compared with standard PCB manufacturing because thicker copper changes trace geometry, spacing requirements, and fabrication conditions.
Important design considerations include:
Design Factor
Engineering Consideration
Trace width and spacing
Requires copper thickness compensation
Copper distribution
Avoid excessive imbalance between layers
Clearance
Must consider thicker copper profiles
Impedance control
Requires stack-up-based calculation
Thermal design
Optimize copper planes and heat paths
During DFM review, engineers typically evaluate:
Copper thickness versus minimum trace width
Etching capability
Layer-to-layer registration
Resin filling conditions
Finished board thickness
These high current PCB design guidelines should be confirmed against the proposed copper weight and stack-up during an engineering DFM review. Early communication helps avoid unnecessary redesign during manufacturing.
Which Via Technologies Are Available for Heavy Copper PCB Manufacturing?
Via structures play an important role in heavy copper PCB performance because they influence current flow, thermal transfer, and mechanical reliability.
Available via technologies include:
Through-hole vias
Plated through vias
Thermal via arrays
Large diameter vias
Multiple parallel vias for current distribution
For power applications, engineers often use multiple thermal vias under heat-generating components or create parallel via paths to reduce electrical resistance.
Via design should consider:
Current requirements
Component heat generation
Copper thickness
Assembly conditions
A proper via structure improves both electrical performance and thermal management.
Which Standards and Certifications Apply to Heavy Copper PCBs?
Heavy copper PCB manufacturing for industrial, automotive, medical, and aerospace applications often requires compliance with recognized quality standards.
Qualification and performance specification for rigid PCBs
IPC-A-600
PCB acceptance criteria
ISO 9001
Quality management system
ISO 13485
Medical device applications
IATF 16949
Automotive applications
AS9100D
Aerospace applications
Specific requirements depend on the final application, customer specifications, and industry regulations.
Quality control processes may include:
Electrical testing
AOI inspection
X-ray inspection when required
Dimensional inspection
Copper thickness verification
What Is the Typical Lead Time for Heavy Copper PCB Production?
Heavy copper PCB lead time depends on copper thickness, layer count, board complexity, testing requirements, and production volume. Review our PCB lead-time guidance as a planning reference; the quotation confirms the actual schedule.
Typical production stages include:
Production Stage
Time Consideration
Engineering review
Based on design complexity
Prototype production
Depends on copper thickness and stack-up
Volume production
Based on quantity and process requirements
Compared with standard PCB production, heavy copper boards may require additional process controls, including:
Special lamination conditions
Copper thickness verification
Additional inspection steps
Manufacturing feasibility review
Providing complete design information during quotation helps shorten engineering evaluation time.
Recommended information includes:
Gerber files
Layer stack-up
Copper thickness requirements
Current load requirements
Application environment
What Design Guidelines Should Be Followed for 100 oz+ Heavy Copper PCBs?
100 oz+ heavy copper PCB requests require project-specific feasibility review because extremely thick copper affects electrical performance, manufacturing processes, and mechanical characteristics. This section provides design inputs for evaluation and does not state an unconditional production capability.
Key design guidelines include:
Optimize copper distribution
Large differences in copper area between layers can create lamination challenges and affect board flatness. Balanced copper distribution improves manufacturing stability.
Consider current path design
High-current paths should use:
Wider copper areas
Shorter current routes
Multiple copper layers when required
Optimized connection points
Plan thermal management early
High-power applications should consider:
Large copper planes
Thermal vias
Heat spreading structures
Component placement strategy
Complete DFM review before production
For 100 oz+ designs, customers should provide:
Maximum current requirement
Operating temperature
Mechanical dimensions
Layer stack-up preference
Reliability requirements
Early engineering review helps confirm whether the design is suitable for production.
Why Choose EBest Circuit for Heavy Copper PCB Manufacturing?
Selecting a heavy copper PCB supplier requires more than checking the maximum copper thickness. Manufacturing experience, engineering support, and process control directly affect final PCB reliability.
EBest Circuit provides:
Heavy copper PCB manufacturing capability
Custom multilayer PCB solutions
Mixed copper stack-up support
Engineering DFM review
Prototype and production support
PCB assembly integration capability
With more than 20 years of PCB manufacturing experience, EBest Circuit supports customers from initial design evaluation through PCB production and PCBA assembly.
For heavy copper PCB projects, contact sales@bestpcbs.com with your Gerber files, copper requirements, or application details.
Frequently Asked Questions About Heavy Copper PCBs
What copper thickness is considered a heavy copper PCB?
Heavy copper PCBs generally refer to boards using copper thickness above standard PCB levels, commonly starting from 3 oz copper and extending to much higher copper weights depending on the application.
Can you manufacture 100 oz copper PCB?
100 oz+ copper PCB requests require project-specific engineering review. Feasibility can be confirmed only after board size, layer structure, copper distribution, insulation, drilling, plating, and reliability requirements are evaluated.
What applications use heavy copper PCBs?
Heavy copper PCBs are commonly used in power supplies, battery systems, EV equipment, industrial controls, renewable energy systems, and high-current electronics.
What materials are recommended for heavy copper PCBs?
High Tg FR-4, suitable prepreg systems, and thermal management materials are commonly selected based on operating temperature and reliability requirements.
Can heavy copper PCBs include controlled impedance designs?
Yes. Controlled impedance can be considered when heavy copper layers are combined with appropriate dielectric thickness and stack-up planning.
What files are needed for heavy copper PCB quotation?
Customers should provide Gerber files, layer stack-up information, copper thickness requirements, board dimensions, quantity, and application details.
Request a Heavy Copper PCB Manufacturing Review
Whether you need a standard heavy copper PCB or want feasibility feedback on a 100 oz+ high-current concept, EBest Circuit can review your design requirements and provide manufacturing recommendations.
Send your PCB files or technical requirements to sales@bestpcbs.com for engineering evaluation and quotation.
A high voltage PCB has to do more than carry a higher electrical potential. Its layout, insulation system, laminate, conductor geometry, surface condition, and manufacturing tolerances all influence whether the finished board can operate safely without arcing, surface tracking, insulation breakdown, or premature field failure.
EBest Circuit supports high-voltage PCB fabrication and PCBA projects from prototype through production. For projects involving special insulation spacing, heavy copper, controlled dielectric thickness, isolation slots, or unusual stack-ups, send your Gerber files, stack-up, operating voltage, peak voltage, material requirements, and application information to sales@bestpcbs.com for an engineering review and quotation.
What Is a High Voltage PCB?
A high voltage PCB is a circuit board designed with additional insulation, spacing, material, and layout controls to safely handle elevated voltage differences between conductors.
There is no single PCB-industry voltage threshold above which every circuit automatically becomes a high-voltage PCB. In practical power-electronics work, approximately 300 V to 1,000 V is a useful range where high-voltage spacing and insulation considerations become increasingly important, while properly engineered boards can operate above 1 kV.
Typical applications include:
EV charging and battery systems
Industrial power supplies
Solar inverters
Motor drives
High-voltage test equipment
Medical electronics
Power conversion equipment
Energy storage systems
High-voltage measurement circuits
The key distinction is therefore not simply the number printed beside the voltage rail. A reliable design has to manage insulation coordination across traces, pads, layers, component leads, PCB edges, slots, coatings, and the surrounding environment.
How Much Voltage Can a PCB Handle?
For practical high-voltage PCB design, working voltages around 300–1,000 V are common design territory, while specially engineered PCBs can operate above 1 kV; there is no universal maximum PCB voltage rating.
The actual limit is usually determined by the weakest insulation path rather than by the FR-4 laminate alone.
For example, a laminate may have high dielectric strength while an assembled PCB still fails because two exposed pads are too close, contamination forms a conductive surface path, or an unexpected surge exceeds the designed clearance.
Voltage capability is influenced by:
Working voltage: continuous or repetitive voltage between conductors
Peak voltage: maximum DC or AC peak potential difference
Transient voltage: switching spikes and surge events
Clearance: shortest air path between conductive parts
Creepage: shortest surface path between conductive parts
Dielectric thickness: insulation between PCB layers
Material CTI: resistance to surface tracking
Altitude: lower air pressure reduces air insulation capability
Pollution and moisture: contamination can reduce surface resistance
For design and RFQ purposes, it is therefore more useful to specify working voltage + peak/transient voltage than to state only “1,000 V PCB.”
What Is the Difference Between Creepage and Clearance in High Voltage PCB Design?
Clearance is the shortest distance through air between two conductive parts, while creepage is the shortest distance along an insulating surface.
Parameter
What It Measures
Main Failure Risk
Clearance
Shortest path through air
Arcing / air breakdown
Creepage
Shortest path along an insulating surface
Surface tracking
Solid insulation
Path through dielectric material
Dielectric breakdown
Suppose two high-voltage pads are separated by a routed slot. The slot can substantially lengthen the surface path and therefore increase creepage, but the shortest air path must still be checked separately for clearance.
This distinction matters because the two distances are determined differently. Clearance is strongly influenced by transient voltage and altitude, while creepage depends heavily on working voltage, pollution degree, and the CTI of the insulating material.
How Do You Determine High Voltage PCB Clearance and Creepage?
As a practical example, at 400 V RMS, IEC 60664-1 gives a creepage reference of about 2.0 mm for Pollution Degree 2 and Material Group I, but the requirement increases to about 4.0 mm for Material Group III.
That difference is why voltage alone cannot determine the final spacing.
Typical IEC 60664-1 creepage references for Pollution Degree 2 are:
Working Voltage
Material Group I
Material Group II
Material Group III
400 V RMS
2.0 mm
2.8 mm
4.0 mm
800 V RMS
4.0 mm
5.6 mm
8.0 mm
1,000 V RMS
5.0 mm
7.1 mm
10.0 mm
These values illustrate how strongly material tracking performance can affect creepage.
The design sequence should be:
Determine the actual working voltage.
Identify the maximum transient or impulse voltage.
Define whether the insulation is functional, basic, supplementary, or reinforced.
Determine the pollution degree.
Check the laminate CTI and material group.
Account for operating altitude.
Apply the requirements of the relevant end-product standard.
Clearance follows a different calculation path.
For example, typical IEC 60664-1 basic-insulation clearance values at up to approximately 2,000 m include:
Required Impulse Voltage
Typical Minimum Clearance
0.5 kV
0.2 mm
1.5 kV
0.5 mm
2.5 kV
1.5 mm
4.0 kV
3.0 mm
6.0 kV
5.5 mm
This demonstrates why a 400 V circuit cannot automatically be assigned “a 400 V clearance.” Its required clearance may instead be controlled by a 2.5 kV, 4 kV, or higher impulse requirement.
What High Voltage PCB Trace Spacing Should You Use?
For external uncoated conductors, a useful PCB design reference is approximately 1.25 mm at 151–300 V peak and 2.5 mm at 301–500 V peak; at 1,000 V, the spacing reaches about 5.0 mm under the familiar IPC external-uncoated conductor rule.
A practical reference table is:
Voltage Difference, DC or AC Peak
External Uncoated Conductor Spacing
31–150 V
0.60 mm
151–300 V
1.25 mm
301–500 V
2.50 mm
600 V
≈3.0 mm
800 V
≈4.0 mm
1,000 V
≈5.0 mm
For values above 500 V, the external-uncoated reference increases by approximately 0.005 mm per volt above 500 V.
For example:
1,000 V: 2.5 mm + (500 × 0.005 mm) = 5.0 mm
IPC-2221C is the current IPC-2221 revision. It retains conductor-spacing categories while refining areas such as altitude, vacuum operation, and coating definitions, so the current standard should be checked when establishing released design rules.
These PCB conductor-spacing values should not be treated as the final safety clearance for every product. Medical, mains-powered, industrial, automotive, or reinforced-insulation designs may require greater spacing under their applicable IEC or UL safety standard.
Designers should also check more than trace-to-trace spacing:
trace to pad
pad to pad
copper to board edge
trace to mounting hole
trace to chassis
copper to exposed component lead
high-voltage to low-voltage plane
outer-layer to inner-layer conductor
The correct design value is the minimum finished-board distance after manufacturing tolerance, not merely the nominal CAD spacing.
Which Materials Are Best for a High Voltage PCB?
High-CTI FR-4 is suitable for many high-voltage PCBs, while specialized high-voltage laminates become more attractive when surface tracking, humidity, thermal stress, or insulation reliability is more demanding.
The most important properties include:
Material Property
Why It Matters
CTI
Resistance to conductive surface tracking
Dielectric strength
Resistance to breakdown through insulation
Moisture resistance
Helps preserve insulation in humid environments
CAF resistance
Reduces conductive filament reliability risk
Tg
Influences thermal dimensional stability
Td
Indicates thermal decomposition behavior
Resin system
Affects insulation and processing behavior
Z-axis stability
Important for multilayer reliability
CTI is not the same as dielectric strength.
Dielectric strength concerns breakdown through the insulating material.
CTI evaluates resistance to conductive tracking across its surface.
This is why two FR-4 materials with similar dielectric strength can require different creepage distances when their CTI classifications differ.
For demanding designs, specifying only “FR-4” is therefore insufficient. The RFQ should identify either the laminate grade or the required CTI, thermal, flammability, and insulation properties.
How Should You Plan the Stack-Up for a High Voltage PCB?
A high-voltage stack-up should first separate HV and low-voltage domains with controlled dielectric thickness, rather than simply adding layers around an existing layout.
The exact dielectric thickness cannot be reduced to one universal number because it depends on the required solid-insulation voltage withstand, laminate system, insulation class, and applicable product standard.
The stack-up should define:
dielectric thickness between high-voltage layers
high-voltage-to-low-voltage layer separation
copper thickness
material dielectric properties
resin content
finished board thickness
internal plane clearances
via structures crossing voltage domains
Internal copper is surrounded by solid dielectric, so its insulation mechanism differs from exposed surface copper.
Avoid placing a low-voltage or grounded plane immediately underneath a high-voltage node unless the vertical insulation path has been intentionally evaluated.
High-current high-voltage designs need another check. Increasing copper weight can reduce conductor resistance, but heavier copper also changes etching capability, conductor spacing, resin fill, dielectric construction, and finished board thickness.
For unusual HV constructions, stack-up review should therefore happen before final routing, not after the Gerber files are complete.
What Are the Key High Voltage PCB Layout Guidelines?
The most effective layout rule is to create clearly separated HV and LV zones and maintain the required isolation distance around the complete boundary on every copper layer.
Useful layout practices include:
Separate HV and SELV/low-voltage areas.
Maintain the isolation boundary on every copper layer.
Avoid sharp copper points in high-electric-field regions.
Use smooth trace and copper transitions where practical.
Keep HV copper away from uncontrolled PCB edges.
Include vias and plated holes when checking spacing.
Avoid unnecessary test points inside HV areas.
Keep contamination-sensitive regions accessible for cleaning.
Check component body and lead spacing.
Prevent copper pours from entering isolation gaps.
A common design error is creating a large visible clearance on the top layer while an internal copper plane extends underneath the same isolation barrier.
Another occurs around components. The traces may meet the intended rule while transformer pins, connector contacts, heat sinks, screws, or component leads create a shorter path.
A high-voltage layout review should therefore inspect the finished electrical assembly, not only individual traces.
When Should You Use Isolation Slots, Barriers, or Conformal Coating?
Use an isolation slot when PCB area is limited and additional creepage is needed; use barriers when the physical insulation path needs to be extended; use conformal coating mainly when environmental contamination or moisture must be controlled.
These three methods solve different problems.
Isolation slots interrupt the direct PCB surface path and can significantly increase creepage without requiring the same increase in board width.
Barriers physically extend or separate insulation paths and may also help prevent contamination from bridging conductive regions.
Conformal coating protects the PCB from humidity, dust, chemicals, and surface contamination.
Coating performance depends on:
coating material
thickness
adhesion
coverage
cure quality
pinholes
component shadowing
operating environment
applicable standard
Do not assume that ordinary solder mask or conformal coating automatically allows a safety clearance to be reduced.
If an isolation slot is safety-critical, specify its finished minimum width, position, and tolerance on the manufacturing documentation rather than relying only on nominal CAD geometry.
Which Standards Apply to High Voltage PCB Design?
For general PCB design, IPC-2221C is a key reference; for insulation coordination, IEC 60664-1 is one of the most important standards, while the final equipment standard determines the binding safety requirement.
Standard
Typical Relevance
IPC-2221C
Generic printed board design and conductor spacing
IEC 60664-1
Clearance, creepage, insulation coordination
IEC 62368-1
AV and ICT equipment
IEC 60601-1
Medical electrical equipment
UL 796
Printed wiring boards
Product-specific IEC/UL standards
Final equipment safety requirements
The key point is that an IPC spacing table does not automatically prove product safety compliance.
A medical device, EV charger, industrial controller, mains power supply, or ICT product may require different insulation levels even if their PCB operating voltages appear similar.
What Manufacturing Factors Matter for High Voltage PCBs?
The most critical manufacturing requirement is that the finished PCB must preserve the minimum insulation distances assumed by the designer after etching, drilling, routing, lamination, and registration tolerances are included.
Key controls include:
Copper geometry: etching must not reduce critical spacing.
Copper-to-edge distance: routing tolerance must be included.
Isolation slots: finished dimensions must meet the required minimum.
Dielectric thickness: critical insulation layers must match the approved stack-up.
Material control: laminate substitutions require engineering review.
Surface cleanliness: ionic contamination can weaken surface insulation.
Solder mask registration: misalignment may expose copper.
Routing and drilling accuracy: holes and slots can alter creepage paths.
Lamination quality: voids and delamination are undesirable in stressed dielectric structures.
Traceability: safety-related products may require controlled material and process records.
For example, if a design requires a 2.50 mm finished minimum conductor spacing, drawing two features exactly 2.50 mm apart in CAD leaves no manufacturing tolerance.
This is why high-voltage fabrication notes should clearly distinguish between the nominal design dimension and the minimum finished-board requirement. That distinction helps ensure normal fabrication tolerances do not reduce critical spacing below the required minimum.
How Should a High Voltage PCB Be Tested?
At minimum, a high-voltage PCB should receive normal open/short electrical testing; projects with safety-related insulation commonly add insulation-resistance and dielectric-withstand, or hipot, testing according to the product specification.
Depending on the application, verification may include:
open/short electrical test
insulation resistance test
dielectric withstand / hipot test
dimensional inspection of isolation gaps
isolation-slot inspection
cleanliness testing
conformal-coating inspection
functional testing at operating voltage
first-article validation
A hipot test applies a specified voltage between isolated regions and checks whether the insulation can withstand that electrical stress without unacceptable leakage or breakdown.
There is no responsible universal rule such as:
“Test every 1,000 V PCB at 2,000 V.”
The correct hipot voltage and duration come from the end-product standard or approved test specification.
The test document should define:
test voltage
AC or DC
duration
ramp rate
leakage-current limit
test points
pass/fail criteria
For assembled boards, PCB-only testing may not be enough. Connectors, component leads, heat sinks, screws, cables, and other hardware can create shorter insulation paths than the bare board itself.
What High Voltage PCB Design Mistakes Should You Avoid?
The most common high-voltage PCB mistake is choosing spacing from nominal operating voltage alone instead of evaluating peak voltage, creepage, clearance, environment, and manufacturing tolerance together.
Other common problems include:
Confusing clearance with creepage. Increasing the surface path does not automatically increase the air path.
Ignoring altitude. Above approximately 2,000 m, IEC insulation calculations may require clearance correction.
Selecting laminate only by dielectric strength. CTI, moisture resistance, thermal behavior, and contamination also matter.
Assuming solder mask provides reinforced insulation. This depends on the construction and applicable safety standard.
Ignoring internal copper. An outer-layer isolation zone can still contain a hidden plane violation.
Leaving sharp copper features in HV regions. Sharp geometry can increase local electric-field concentration.
Checking PCB traces but not components. Leads, terminals, heat sinks, connectors, and hardware must also maintain isolation.
Designing exactly to the minimum spacing. Fabrication tolerances must be added before design release.
A useful high-voltage design review question is therefore:
Does the finished and assembled product maintain the required insulation under its actual voltage, transient, altitude, contamination, manufacturing tolerance, and service conditions?
FAQs About High Voltage PCB
What voltage is considered high voltage on a PCB?
There is no universal PCB threshold, but approximately 300 V and above is a useful practical point at which clearance, creepage, transients, insulation, and environmental conditions deserve explicit review. Designs in the 300–1,000 V range are common high-voltage PCB territory, while boards above 1 kV are feasible with appropriate engineering.
How much clearance does a high voltage PCB need?
For external uncoated PCB conductors, a useful IPC reference is about 1.25 mm for 151–300 V peak and 2.50 mm for 301–500 V peak, increasing to approximately 5.0 mm at 1,000 V under the external-conductor rule. Product-safety requirements can require larger values.
What is the difference between creepage and clearance?
Clearance is the shortest path through air, while creepage is the shortest path along an insulating surface.
Is FR-4 suitable for high voltage PCBs?
Yes. High-CTI FR-4 is suitable for many 300–1,000 V-class PCB applications, provided its CTI, dielectric construction, thermal performance, creepage, clearance, and end-product requirements are appropriate.
Does conformal coating increase voltage isolation?
It can improve environmental protection and surface insulation performance, but it does not automatically justify smaller safety spacing. The coating material, coverage, process qualification, and applicable standard must support the reduction.
How does altitude affect PCB clearance?
Clearance normally increases with altitude because air density decreases. Above approximately 2,000 m, the applicable standard may require an altitude correction factor.
Can isolation slots increase creepage distance?
Yes. A correctly placed slot can substantially increase creepage without requiring the same increase in PCB width, although clearance must still be checked separately.
If you are developing a high-voltage PCB and want the fabrication capability checked before prototype release, send your Gerber files, stack-up, working voltage, peak or surge voltage, copper weight, material requirements, critical isolation dimensions, and applicable standard to sales@bestpcbs.com. EBest Circuit can review stack-up manufacturability, critical spacing, isolation slots, copper geometry, dielectric construction, and other fabrication-sensitive features before quotation and production.
A GPS navigation PCB assembly combines a GPS or multi-constellation GNSS receiver with its antenna interface, processor, power supplies, memory and product communication circuits. It converts weak satellite signals into position and timing data that the host product can use for navigation, tracking or control.
Successful production depends on more than assembling the GNSS module. RF routing, power noise, board stackup, component placement, firmware and the functional test method must work together. EBest Circuit supports design review, PCB fabrication, component sourcing, SMT assembly, programming and customer-defined testing from prototype through repeat production.
Are you worried about your GPS navigation PCB assembly project?
Could antenna placement, enclosure metal or an unreviewed RF substitution reduce receiver margin after assembly?
Could power ripple, switching nodes or high-speed digital circuits interfere with acquisition or communication?
Could incomplete programming and test requirements produce a prototype that cannot be released confidently for repeat builds?
With over 20 years of experience, EBest Circuit provides one-stop PCB and PCBA manufacturing support from design review and prototyping through repeat production.
Protect receiver margin: We review the submitted stackup, RF feed, matching components, antenna interface and enclosure constraints before PCB release.
Control the assembled configuration: We align the BOM, placement data, power requirements, firmware and assembly drawing so purchasing and production use the same revision.
Build usable release evidence: We coordinate inspection, programming and customer-defined functional checks so prototype results can support the next production decision.
Ready to start your GPS navigation PCB assembly project? Send your PCB data, BOM, placement file, assembly drawing, module and antenna references, quantities and test requirements to sales@bestpcbs.com.
What Is a GPS Navigation PCB Assembly and How Does It Work?
A GPS navigation PCBA receives satellite signals, calculates or relays positioning data and passes that data to the host product. GPS is one GNSS constellation; many current receivers can also use Galileo, BeiDou or GLONASS. The approved module specification determines which constellations, interfaces and operating modes apply to the product.
The signal path normally runs from the GNSS antenna through an RF feed and matching network to the receiver. The receiver outputs navigation or timing data to an MCU or processor, which exchanges information with the display, cellular modem, CAN network, USB port or another host interface. Power-management circuits supply the receiver and, when used, an active antenna. Before assembly release, verify the module interface, antenna path and required output messages against the approved schematic and module documentation.
Where Are GPS Navigation PCB Assemblies Used?
GPS navigation PCB assemblies are used wherever a product must determine, report or act on location, speed or precise timing. The application changes the mechanical environment, interfaces, power states and acceptance tests that the manufacturer must plan.
Automotive navigation and telematics: The PCBA may exchange data with vehicle networks, displays, cellular modules and sensors while operating near chargers, motors and other noise sources.
Fleet and asset tracking: Low-power operation, cellular connectivity, enclosure size and antenna placement often control the design and test conditions.
Marine and industrial positioning: Connector sealing, corrosion exposure, cable routing and external-antenna interfaces can become part of the manufacturing package.
UAV and agricultural equipment: Vibration, power-converter noise, orientation and communication interfaces must be defined for the intended installation.
Portable navigation products: Battery management, compact layout, display activity and enclosure interaction can affect both assembly and functional validation.
What Components Are Integrated on a GPS Navigation PCB?
The board combines the GNSS signal chain with processing, power and product interfaces. Each functional block creates a distinct placement, sourcing or verification task, so the design package should identify the exact component and the evidence required for release.
GNSS receiver: Processes satellite signals and outputs position, velocity or timing data. Production must control the exact part number, package orientation, footprint and approved substitution boundary.
RF path: Connects the antenna interface, filter, amplifier or matching network to the receiver. Review the feed geometry, reference plane, keepout, matching-component identity and connector condition.
MCU or processor: Uses navigation data and controls product logic. Release its programming package, clocking, reset behavior and required interfaces with the assembly data.
Power management: Supplies the receiver, processor and active antenna when used. Define the rail sequence, ripple-sensitive loads, regulator placement and measurement points.
Memory and timing: Stores code or configuration and provides timing references. Control the exact device identity, oscillator layout, loading parts and programming data.
Product interfaces: Connect UART, USB, CAN, Ethernet, cellular, Bluetooth or other product circuits. Identify connector orientation, protection parts, routing constraints and functional-test access.
How Do RF Layout and Antenna Integration Affect GPS Performance?
The RF feed must preserve the reference design from the antenna interface to the receiver. Loss, discontinuities, an interrupted return path or coupling from nearby electronics can reduce the usable signal margin before software processes the data.
The selected module and antenna documents remain the controlling sources. The u-blox GNSS antenna integration overview explains why the front-end RF path, interference filtering and antenna environment must be considered together. The actual stackup, antenna and enclosure still require project-specific review.
Preserve the RF feed: Route the specified feed over its reference plane, control transitions and keep the matching network close to the location defined by the reference design.
Protect the antenna zone: Apply the required copper, component and mechanical keepout around the embedded antenna or approved antenna interface.
Control the enclosure boundary: Record nearby metal, cable routes, connector position and antenna orientation because these conditions can change the assembled RF environment.
Restrict substitutions: Mark filters, matching parts, connectors and active-antenna components as do-not-substitute unless engineering approval includes the necessary retest.
Provide inspection access: Define how RF connectors, shield joints and hidden receiver-module joints will be inspected without damaging the feed or antenna contact.
How Should Power Integrity and Digital Noise Be Managed?
The receiver needs a stable supply and physical separation from strong switching and digital noise sources. A board can communicate correctly on the bench yet lose receiver margin when a modem transmits, a display switches or a DC-DC converter enters a different operating mode.
Define the power tree: Identify receiver and active-antenna rails, startup sequence, reset criteria, expected current states and the measurement points used during verification.
Place converters deliberately: Keep switching nodes, inductors and high-current loops away from the RF feed, receiver input and timing components. Use the selected regulator and module guidance to set the boundary.
Apply local decoupling: Place specified capacitors at the intended pins with short return paths so component placement matches the electrical design rather than a generic assembly convention.
Test active noise states: Exercise the processor, display, cellular radio, charger, motor or other integrated loads that can create product-level interference.
Record comparable conditions: Tie results to firmware, antenna, enclosure, supply source and operating mode so changes between builds can be evaluated.
How Should RF, Power and Digital Circuits Be Separated?
Partition the board by current path and noise sensitivity, then preserve continuous return paths between connected functions. Physical separation alone is insufficient if a noisy signal crosses the RF reference area or a plane opening forces return current around the receiver.
Reserve the RF zone: Keep the receiver input, feed, matching network and antenna interface together and away from clocks, switching nodes and high-current connectors.
Contain the power zone: Minimize the hot loop of each switching converter and route its input, switch node and output currents without crossing the RF area.
Control digital routing: Route fast clocks, USB, memory buses and processor interfaces over continuous references and away from the antenna feed.
Place timing parts carefully: Position the crystal or TCXO according to the component reference layout and avoid coupling from switching or high-speed nets.
Plan shielding and test access: Locate shield fences, cans, programming pads and measurement points before routing is frozen so production can inspect and test the board without improvisation.
If a switching return crosses the RF reference area, supply noise can couple into the receiver input and cause slow or intermittent acquisition. Verify the final partition by reviewing current-return paths and repeating receiver tests while converters and high-speed interfaces operate in their defined active states.
What PCB Manufacturing Requirements Matter for GPS and GNSS Boards?
The PCB specification must preserve the RF reference, power return paths and package geometry required by the released design. Layer count or material should not be selected from the application name alone; the stackup, routing density, impedance needs and assembly packages determine the construction.
Stackup and reference planes: Define layer order, dielectric thickness, copper weight and reference planes so controlled routes and return paths match the approved layout.
Controlled features: State any impedance target, trace geometry, coupon or verification requirement that applies to the RF feed or other controlled nets.
Material selection: Use the designer-specified FR-4 or RF material and its approved equivalent boundary. Do not replace material solely from a generic GPS label.
Via and HDI structures: Specify through vias, blind or buried vias, via-in-pad treatment and fill requirements only where routing or package escape requires them.
Surface and dimensional control: Define finish, solder mask, board outline, connector geometry and RF trace-etching requirements that affect assembly or interface fit.
Fabrication evidence: Release the approved stackup, controlled-feature report and any inspection records required for prototype acceptance or repeat orders.
How Is a GPS Navigation PCB Assembly Manufactured?
The process converts one released PCB, BOM and assembly package into an inspected and programmed navigation board. Each operation must protect the GNSS module, RF parts, timing devices, connectors and shields identified by the design.
Verify incoming materials: Match PCB revision, component part numbers, moisture requirements and approved substitutions to the purchase package. Quarantine discrepancies before they enter kitting, and retain the receiving record required by the order.
Print and inspect solder paste: Use the released stencil and paste process for the actual pad geometry and thermal mass. SPI can detect deposit conditions covered by the plan before placement makes the defect harder to isolate.
Place sensitive components: Load the approved program and verify pin-one, connector direction, GNSS module orientation, RF filters, matching parts and timing components. A first-article check should confirm these identities before the run continues.
Reflow the assembly: Establish the profile for the actual board, solder and component limits. Monitor the defined profile evidence because an unrelated board’s profile does not prove suitable heating for the current module or shields.
Inspect soldered joints: Apply AOI to visible conditions and X-ray where hidden joints create a documented risk. Record defects and disposition against the order’s acceptance criteria.
Complete secondary operations: Install through-hole connectors, shields, cables or hardware using the approved drawing. Protect RF contacts and test points from residue or mechanical damage.
Program and functionally test: Load the approved firmware, verify its identity and run the specified electrical and navigation checks. Save the result format required for prototype approval or traceability.
If the order invokes IPC requirements, state the revision and class. IPC distinguishes solder-process requirements in J-STD-001J from post-assembly acceptability in A-610J, as summarized in the IPC assembly standards release.
How Should GPS Navigation PCB Assemblies Be Tested?
Inspection verifies construction, while electrical and functional tests verify the customer-defined behavior. The test plan should separate visible solder evidence, hidden-joint evidence, power and interface checks, firmware control and GNSS operation.
Structural inspection: Use SPI, AOI, visual inspection and X-ray only for the conditions each method can observe. Define package targets, coverage and defect disposition instead of presenting one method as universal.
Electrical checks: Measure specified rails, current states, shorts, opens and interfaces at named points with the fixture revision and pass limits recorded.
Programming control: Verify firmware version, configuration, serialization and programming result before the navigation test begins.
GNSS functional test: Check receiver communication, module status, antenna condition and required positioning outputs under the antenna, enclosure and operating conditions defined by the customer.
Acceptance boundary: Assembly inspection does not certify final positioning accuracy. Product-level performance requires the customer’s defined environment, limits and validation method.
Failure records: Preserve board identity, firmware, antenna state, power state and test setup so the team can distinguish an assembly defect from design, component, software or environmental causes.
How Is a Prototype Validated Before Mass Production?
The prototype stage must close design-transfer, sourcing, assembly and test risks before quantity increases. A board that acquires satellites once is not enough; the release package must show what was built, what changed and how later units will be judged.
Release Area
Prototype Evidence
Volume Decision
Configuration
PCB, BOM, placement data, firmware, antenna and approved substitutions match
Freeze the as-built baseline and open exceptions
Assembly
First-article, solder, connector, shield and hidden-joint results as applicable
Approve the process or require corrective action
Power and interfaces
Startup, reset, rail, current and communication results under defined states
Set the repeatable electrical test limits
GNSS function
Customer-defined antenna, enclosure, operating mode and output results
Approve the functional method and result format
Supply continuity
Approved part numbers, lifecycle risks, alternates and material responsibility
Authorize purchasing for the planned quantity
For pilot and repeat production, carry forward the approved BOM, firmware, assembly notes, test limits and exception record. Any change to the GNSS module, RF components, antenna, enclosure or power architecture should invalidate the affected evidence and trigger the relevant review or retest.
What Common Problems Cause GPS Navigation PCBA Failures?
Most failures can be narrowed by linking the symptom to the RF path, power state, assembled configuration or test environment. Diagnosis should reproduce the reported condition before changing parts or retuning the design.
Weak or unstable reception: Inspect the antenna contact, RF connector, feed continuity, matching-part identity and enclosure changes. Compare the result with the approved antenna condition.
Slow or intermittent acquisition: Measure supply ripple and startup states, confirm firmware identity and repeat the test while defined product circuits are active.
No receiver communication: Check module orientation, solder joints, reset, clock, interface activity and programming configuration before replacing the receiver.
Active antenna fault: Measure the defined bias supply and inspect the protection circuit, connector and cable path under the approved load condition.
Enclosure-only failure: Compare bare-board and enclosure results with the same firmware and power state, then inspect nearby metal, cable routing, orientation and internal radio activity.
What Affects GPS Navigation PCB Assembly Cost and Lead Time?
The cost and schedule for GPS navigation PCB assembly depend on material availability, board complexity, package mix, inspection coverage, programming, fixtures, functional-test time and order quantity. A quote is comparable only when each supplier prices the same released scope.
Component availability: Allocated navigation modules or buyer-restricted parts can determine the material schedule. Approved alternatives and consigned parts change both risk and commercial responsibility.
PCB construction: Layer count, controlled impedance, specified RF material, HDI structures, finish and dimensional requirements affect fabrication cost and schedule.
Assembly complexity: Fine-pitch packages, bottom-terminated parts, shields, RF connectors and mixed SMT/through-hole operations affect tooling, inspection and rework exposure.
Test scope: Fixture design, firmware loading, electrical checks, RF connections and product-specific navigation tests should be quoted explicitly. A lower price that omits agreed evidence is not an equivalent offer.
Prototype learning: Unresolved DFM questions, test-method gaps or unstable BOM revisions lengthen the path to volume release. Closing them in the prototype reduces avoidable changes later.
Order profile: Prototype, pilot and repeat production use different quantities, setup effort and material commitments. Provide the current quantity and forecast instead of requesting one price for an undefined range.
What Files Are Needed for a GPS Navigation PCB Assembly Quote?
An accurate quote needs one released, internally consistent package that identifies what will be fabricated, purchased, assembled, programmed, inspected and tested. Missing or conflicting files force the supplier to make assumptions that later change price or delivery.
PCB data: Gerber or approved intelligent data, drill files, board outline, stackup, material, copper, finish and controlled-feature notes.
BOM: Complete manufacturer part numbers, quantities, approved alternatives, do-not-substitute items and any consigned material.
Placement data: Reference designator, X/Y position, rotation, side and origin convention matching the released assembly drawing.
Assembly drawing: Polarity, connector direction, shields, hardware, special soldering, antenna keepouts and workmanship notes.
Module and antenna references: Relevant datasheets, layout guidance, matching details and approval boundaries for the selected configuration.
Programming package: Firmware identity, programming method, security or serialization inputs and verification output.
Test specification: Fixture interface, power states, measurement points, limits, navigation conditions, sampling or full-test requirement and result format.
Commercial inputs: Prototype and production quantities, target schedule, delivery location, packaging, traceability and required quality records.
Why Choose EBest Circuit for GPS Navigation PCB Assembly?
EBest Circuit gives buyers one project path for PCB fabrication, component sourcing, SMT assembly, programming coordination and customer-defined testing. This reduces handoff gaps between board production, parts and assembly while keeping the approved design and evidence requirements visible.
One-stop PCB and PCBA: Coordinate fabrication, sourcing, SMT, secondary assembly and project records through one manufacturing handoff.
RF-focused manufacturability review: Check submitted stackup, controlled routes, receiver footprint, matching-part placement, shield and connector requirements before release.
GNSS module assembly control: Tie exact module identity, orientation, moisture handling and approved substitutions to the released BOM and drawing.
Programming and test coordination: Build the supplied firmware, fixture, limits and result format into the production package instead of treating testing as an undefined add-on.
Prototype-to-volume continuity: Transfer the approved as-built configuration, exceptions and test evidence into pilot and repeat orders.
Traceable project response: Return DFM questions, sourcing risks and missing evidence against the submitted files so the buyer can close specific release decisions.
FAQs About GPS Navigation PCB Assembly
Q1: Does every GPS navigation board require a controlled-impedance RF trace?
A1:Follow the selected module and antenna reference design. The required feed structure, impedance target and layout depend on the chosen configuration. Specify the approved feed geometry, stackup reference, matching locations and acceptance method in the released PCB data rather than assuming every module uses the same structure.
Q2: Can AOI confirm GPS or GNSS reception?
A2:No, AOI verifies visible assembly conditions. Navigation performance needs a separate customer-approved functional method with the defined antenna, firmware, power state, enclosure and signal environment. Keep the AOI record and functional result separate so each one proves only what it actually checks.
Q3: Can FR-4 be used for a GPS navigation PCB?
A3:Use the material specified by the released stackup and RF design. Many navigation boards may use FR-4, while a design with different loss, frequency or routing constraints may specify another material. Confirm the impedance, geometry and supplier-approved material boundary rather than selecting by product name alone.
Q4: Can EBest source the GPS or GNSS module?
A4:Component sourcing can be included in the project scope. Supply the exact manufacturer part number, approved alternatives and any date-code or traceability requirements for review. Parts that affect RF, timing, firmware or regulatory evidence should remain do-not-substitute unless the approval process says otherwise.
Q5: Can a GPS navigation PCB include cellular, Bluetooth or CAN interfaces?
A5:Yes, when the product architecture and layout support them. Define each interface, its power state, routing constraints and simultaneous operating modes. Wireless transmitters and high-speed circuits should be active during the relevant interference and functional checks.
Q6: Can a module substitution be approved from the footprint alone?
A6:No, mechanical compatibility does not prove functional equivalence. Check electrical, RF, firmware, regulatory, lifecycle and test implications before approving a replacement. Record the approved alternative and any required retest against the affected board and firmware revision.
Q7: Where should the GNSS module be placed on the PCB?
A7:Follow the selected module reference layout and the board’s RF partition. Keep the receiver input and antenna feed away from strong switching and digital noise sources, preserve its reference plane and leave the required antenna or connector boundary intact.
Q8: What makes a GPS navigation PCBA quote change?
A8:Scope changes alter material, setup and test effort. Common causes include BOM revisions, unavailable parts, added inspection, new fixtures, firmware changes, quantity changes and missing acceptance criteria. Compare quotations only after these assumptions and their validity periods are stated in writing.
Q9: Does every navigation PCBA need X-ray inspection?
A9:No, X-ray should follow package and hidden-joint risk. Use it when the GNSS module, processor or another bottom-terminated package requires internal evidence under the inspection plan. Visible joints still need the appropriate visual or optical checks.
Q10: What should buyers send first for a manufacturability review?
A10:Send the complete released PCB and assembly package. Include the BOM, placement data, drawings, module and antenna references, quantities, programming method and test requirements. Consistent revisions let the supplier identify open decisions without rebuilding design intent from separate emails.
Conclusion
A production-ready navigation PCBA connects receiver architecture, RF integration, power integrity, PCB construction, assembly and functional testing under one approved configuration. That connection lets engineering diagnose real product risks and gives purchasing a comparable basis for scope, price, lead time and repeat-production evidence.
EBest Circuit can review your project from PCB fabrication and component sourcing through prototype assembly, programming coordination and repeat production. Send the Gerber or approved intelligent PCB data, BOM, placement file, assembly drawing, module and antenna references, quantities and test specification to sales@bestpcbs.com for a project-specific DFM review and quotation.
This website uses cookies to enhance your experience, remember your preferences, and help us understand how visitors use our site. You can accept all cookies, reject non-essential cookies, or manage your settings.
This website uses cookies to improve your experience while you navigate through the website. Out of these cookies, the cookies that are categorized as necessary are stored on your browser as they are essential for the working of basic functionalities of the website. We also use third-party cookies that help us analyze and understand how you use this website. These cookies will be stored in your browser only with your consent. You also have the option to opt-out of these cookies. But opting out of some of these cookies may have an effect on your browsing experience.
Necessary cookies are absolutely essential for the website to function properly. These cookies ensure basic functionalities and security features of the website, anonymously.
Cookie
Duration
Description
cookielawinfo-checkbox-analytics
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytics".
cookielawinfo-checkbox-functional
11 months
The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional".
cookielawinfo-checkbox-necessary
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Necessary".
cookielawinfo-checkbox-others
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Other.
cookielawinfo-checkbox-performance
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance".
viewed_cookie_policy
11 months
The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data.
Functional cookies help to perform certain functionalities like sharing the content of the website on social media platforms, collect feedbacks, and other third-party features.
Performance cookies are used to understand and analyze the key performance indexes of the website which helps in delivering a better user experience for the visitors.
Analytical cookies are used to understand how visitors interact with the website. These cookies help provide information on metrics the number of visitors, bounce rate, traffic source, etc.
Advertisement cookies are used to provide visitors with relevant ads and marketing campaigns. These cookies track visitors across websites and collect information to provide customized ads.