PCB manufacturing PCB manufacturing
Home > Blog

PCB Layout

When to Use an Inductor vs Capacitor?
Tuesday, September 15th, 2026

The practical inductor vs capacitor choice starts with the circuit variable that is misbehaving. Choose a capacitor first when you need to hold a voltage steady, supply a brief current pulse, bypass high-frequency noise, smooth voltage ripple, or pass AC while blocking DC. Choose an inductor first when you need to limit the rate of current change, store energy in a switching converter, or block high-frequency current in series with a line. Use both when one part cannot meet the required attenuation or when the circuit needs a tuned response.
inductor vs capacitor, shielded power inductor and aluminum capacitor mounted on a PCB

A capacitor opposes a rapid change in voltage, while an inductor opposes a rapid change in current. That first choice still has to survive the part’s impedance curve, applied bias, temperature, source and load impedance, and PCB loop parasitics.

What Is the Main Difference Between an Inductor and a Capacitor?

The main inductor vs capacitor difference is the variable each part controls: capacitance primarily controls node voltage, while inductance primarily controls path current. Their energy storage, connection, and parasitic limits explain when that rule works and when it does not.

Selection Factor Capacitor Inductor
Controlled variable Opposes rapid voltage change Opposes rapid current change
Energy storage Electric field, E = ½CV² Magnetic field, E = ½LI²
Usual connection Across a rail or from a node to a reference; in series for AC coupling In series with the current path
Frequency trend Ideal reactance falls as frequency rises Ideal reactance rises as frequency rises
Typical use Rail droop, voltage ripple, bypassing, AC coupling Current ripple, converter energy storage, series filtering
Key limit DC-bias loss, ESR, ESL, ripple current Saturation, DCR, core loss, temperature rise

These differences identify the component class, not the finished part. The impedance curve, applied bias, temperature, source and load impedance, and PCB current loop still determine whether the selected value will work.

When Should You Use a Capacitor?

Choose a capacitor first when the circuit needs local charge or a low-impedance path that controls voltage at a node. Match the capacitor to the duration and frequency of the problem rather than increasing capacitance blindly.
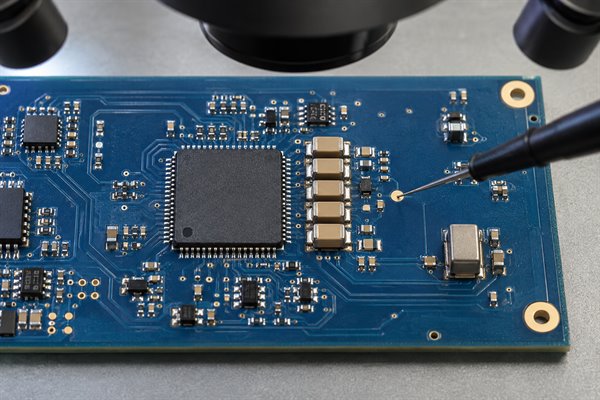
inductor vs capacitor, probe checking decoupling capacitors beside a microcontroller on a blue PCB
  • IC rail droop: Place a decoupling capacitor close to the power pin when a switching edge pulls current faster than the upstream supply can respond. Check the rail at the device pin; effective capacitance, ESL, and loop length matter more than the printed capacitance alone.
  • Longer load transients: Use bulk capacitance when the current step lasts beyond the useful range of a small ceramic capacitor. Estimate the starting value with C ≈ IΔt/ΔV, then include ESR step, tolerance, temperature, and the regulator response time.
  • Output voltage ripple: Use a capacitor to absorb the AC component of a rectifier or converter output. Confirm ripple-current rating and ESR heating, and make sure the regulator remains stable with the chosen capacitance and ESR range.
  • High-frequency bypass: Use a small capacitor when noise must return locally to a reference plane instead of travelling along the power network. Verify the impedance near the interference frequency and keep the mounting and via inductance low.
  • AC coupling: Put a capacitor in series when an AC signal must pass between stages with different DC bias. Set the capacitance from the lowest wanted signal frequency and the surrounding impedance, then check startup transients and distortion.
  • Timing or short hold-up: Use an RC network when a changing capacitor voltage provides the timing or temporary energy. Leakage, input bias current, dielectric behavior, and tolerance set the real timing accuracy.

A larger capacitor can increase inrush current, delay startup, or disturb a control loop. If the problem is a fast event at one IC, placement and loop inductance may matter more than adding bulk capacitance elsewhere on the board.

When Should You Use an Inductor?

Choose an inductor first when the circuit must shape current, transfer energy between switching states, or create series impedance without wasting the required DC current in a resistor.
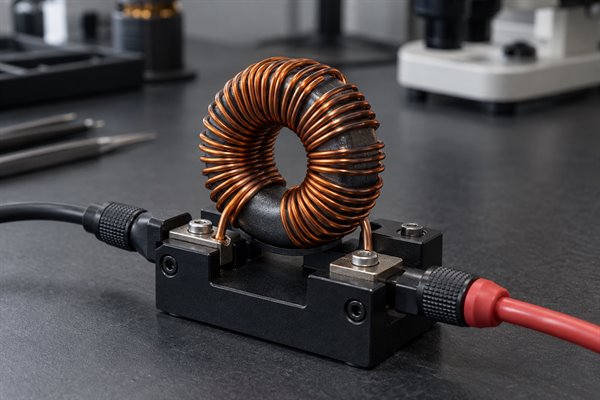
inductor vs capacitor, copper-wound toroidal inductor secured in an electronics test fixture
  • Switching-converter energy transfer: Buck, boost, and related converters use inductance to set the current slope. Derive the starting value from topology, input and output voltage, switching frequency, and allowed ripple; then check peak current against the saturation curve.
  • Current-ripple control: Add series inductance when the load or converter cannot tolerate a large change in current each switching cycle. Measure or calculate peak-to-peak ripple and verify DCR loss, core loss, RMS current, and temperature rise.
  • Power-line filtering: Use an inductor when unwanted current must be impeded while DC power continues through the line. Check the impedance at the actual noise frequency and the DC drop at full load.
  • RF bias isolation: Use an RF choke to feed bias while keeping the RF signal out of the supply path. The useful band must remain below self-resonance and within the current rating; nominal inductance alone is not enough.
  • Lossy noise suppression: Consider a ferrite bead instead when high-frequency attenuation is needed but magnetic energy storage is not. Compare impedance-versus-frequency and DC-bias curves because a bead that looks effective at zero bias can weaken under load.
  • Tuning and matching: Use an inductor with capacitance when a resonant or impedance-matching network is intentional. Include component Q, tolerance, pads, vias, and nearby copper in the frequency check.

Do not place a series inductor in front of a fast load merely because the rail is noisy. It can restrict the transient current the load needs. If the observed failure is a local voltage dip at an IC pin, start with the capacitor and its return path.

How Do Inductors and Capacitors Behave Differently in DC and AC Circuits?

At steady-state DC, an ideal capacitor has finished charging and carries no continuous current, while an ideal inductor carries constant current. During startup or a transient, however, capacitor voltage cannot change instantly and inductor current cannot change instantly. That is why a capacitor can support a rail during a brief load step and an inductor can control current rise in a converter.

Frequency changes their ideal impedance in opposite directions. Capacitive reactance is XC = 1/(2πfC), so it falls as frequency rises. Inductive reactance is XL = 2πfL, so it rises as frequency increases. This supports the familiar arrangement of a shunt capacitor for high-frequency node noise and a series inductor for high-frequency line current.

Real parts stop following the ideal trend near self-resonance. Capacitor ESL eventually dominates, and inductor winding capacitance eventually dominates. Read the manufacturer’s impedance curve at the operating frequency and applied bias before relying on the nominal C or L value.

When Should You Use Both an Inductor and a Capacitor?

Use an LC network when one component cannot meet the attenuation or ripple target and the circuit can tolerate the added resonance and transient behavior. Each common use needs a different check.

  • Converter output filtering: Add C to hold the output voltage and L to limit switching-current ripple when either part alone would require an impractical value. Check output ripple, load-step response, inductor peak current, and control-loop stability.
  • Converter input filtering: Use LC filtering when switching current must be kept out of the upstream supply or cable. Compare filter impedance with converter input impedance and add damping when simulation or measurement shows peaking.
  • Second-order low-pass filtering: Combine series L and shunt C when the required roll-off exceeds what a single reactive element can provide. Define passband loss and stopband attenuation first, then verify the response with real ESR, DCR, source impedance, and load impedance.
  • Resonant or tuned networks: Use both when the intended function depends on resonance or impedance matching. Start with f0 = 1/(2π√LC), then include tolerance, Q, package parasitics, pads, and layout in the final frequency check.
  • Ringing control: Treat an undamped LC peak as a design problem, not as extra filtering. If a load step or frequency sweep shows overshoot, add controlled damping or change the L/C values or topology before release.

The extra order improves attenuation only when the network is stable and correctly damped. Prototype measurements should confirm both frequency response and transient response under the expected source and load conditions.

How Do You Choose Between an Inductor and a Capacitor for Common Circuit Problems?

Match the component to the failing variable, then verify the choice with the measurement or datasheet curve that can disprove it. This keeps the first component choice tied to an observable circuit result.

Circuit Condition Preferred Component Validation Check
IC supply dips during switching Local capacitor Measure droop at the power pin; inspect ESR step and loop inductance
Converter output has voltage ripple Capacitor Check ripple current, ESR heating, and regulator stability
Switching current ripple is excessive Inductor Check ripple, peak current, saturation margin, and temperature
Converter must store and transfer energy Inductor Verify peak and RMS current, DCR loss, and core loss
Signal must pass without its DC bias Series capacitor Check low-frequency loss, bias conditions, and startup transient
High-frequency noise travels along a power line Inductor or ferrite bead Compare loaded impedance, DC drop, resonance, and attenuation
One part misses the attenuation target LC network Sweep frequency and load; check peaking, damping, and stability

What Should You Check When Selecting a Real Capacitor or Inductor?

Choose the nominal value only after defining the worst-case voltage, current, frequency, temperature, and allowed circuit error. Then use the following checks to remove parts that will fail under bias or on the assembled PCB.

  • Required capacitor value: Calculate from the actual job: transient current and allowed droop, filter impedance, coupling corner frequency, or timing interval. Use the manufacturer’s DC-bias curve to confirm the effective capacitance at the operating voltage.
  • Capacitor loss and frequency limit: Check ESR for ripple heating and damping, ESL for fast-transient performance, ripple-current rating for power applications, and self-resonant frequency for bypassing. A higher nominal capacitance can perform worse at the noise frequency if the package and mounting add too much inductance.
  • Inductor peak-current margin: Calculate the highest instantaneous current, including ripple and startup or fault conditions. Confirm inductance at that current and keep the peak below the manufacturer’s saturation limit with the required design margin.
  • Inductor thermal loss: Use RMS current, DCR, switching frequency, and the manufacturer’s core-loss or temperature-rise data. Passing the saturation-current rating does not prove that winding and core temperature are acceptable.
  • Operating range: Check tolerance, temperature dependence, aging where applicable, and impedance versus frequency for both parts. Validate the worst operating corner rather than comparing only room-temperature headline ratings.
  • PCB implementation: Keep a decoupling loop short and its return path direct. Give a power inductor enough copper for current and heat, and separate its magnetic field and switching node from feedback, sensor, and RF traces. Confirm footprint, polarity, height, keep-outs, and assembly clearances against the exact manufacturer part.

The final check is a measurement at the point where the circuit can fail: rail droop at the IC pins, ripple at the converter output, current at the inductor, or attenuation across the filter. A part number is qualified only when the operating waveform and temperature remain inside its real limits.

Common Questions About Inductors and Capacitors

Q1: Can a capacitor replace an inductor?

A1: Not when the circuit needs controlled current ramping or magnetic energy transfer, as in a buck or boost power stage. A capacitor may reduce voltage ripple in the same converter, but it cannot perform the inductor’s current-control function.

Q2: Can an inductor replace a capacitor?

A2: Not for local rail support, AC coupling, or a shunt bypass path. A series inductor can impede noise current, but it cannot provide the immediate local charge that holds an IC supply voltage steady.

Q3: Which component is better for filtering noise?

A3: Choose by noise path. Use a capacitor when unwanted energy should be shunted from a node, an inductor or ferrite bead when unwanted current should be blocked in a line, and an LC network when the attenuation target requires both actions.

Q4: Why use a ferrite bead instead of an inductor?

A4: A ferrite bead is usually selected to dissipate high-frequency noise, while a power or RF inductor is selected for energy storage, current control, or a higher-Q reactance. Compare the bead’s impedance-versus-frequency curve under DC bias before using it in a supply filter.

Q5: Why are capacitors usually connected in parallel and inductors in series?

A5: A parallel capacitor can supply or absorb current at a node while holding its voltage, whereas a series inductor directly opposes a changing current in the path. These are common arrangements, not universal rules; AC-coupling capacitors are a familiar series exception.

Choose C for a voltage problem, L for a current problem, and LC when the circuit needs both series impedance and a shunt path. Then test the decision at the actual frequency, bias, current, temperature, source and load impedance, and PCB layout.

If the choice is still uncertain after calculation—or a prototype shows rail droop, excessive current ripple, filter ringing, or unexpected heating—send the actual design rather than a generic part request. Email sales@bestpcbs.com with your schematic, PCB files, BOM with exact part numbers or approved alternatives, operating voltage, peak and RMS current, switching or noise frequency, ripple or attenuation target, quantity, target date, and test requirements. EBest Circuit can use those inputs for a free DFM and component-sourcing review focused on footprint compatibility, current paths, thermal exposure, layout-sensitive noise, and substitution risks before the design is released.
You may also like

What Is a Bulk Capacitor and How to Calculate It?
Tuesday, September 8th, 2026

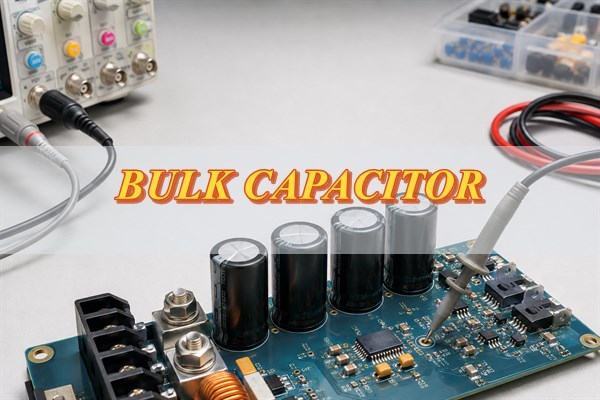
A bulk capacitor is an energy reservoir connected to a power rail. It supplies current when a load changes faster than the upstream source can respond, and it can absorb energy when the load releases current back onto the rail. The result is less voltage droop, overshoot, and low-frequency ripple at the circuit that must remain powered.
Calculating the value begins with the current-versus-time event, not a familiar capacitance such as 470 µF or 2,200 µF. The designer must define the current shortfall, its duration, the permitted rail movement, and the non-ideal losses in the capacitor and PCB path. The nominal value is selected only after those inputs are known, then confirmed on the assembled board.
Bulk capacitor, electrolytic capacitor bank on a power electronics PCB under bench evaluation

What Is a Bulk Capacitor and What Does It Do?

A bulk capacitor stores enough local charge to support a rail during a relatively high-energy event. The event may be a processor load step, a radio transmission burst, motor startup, a long cable feeding a board, a rectified supply between charging peaks, or energy returned by an inductive load.

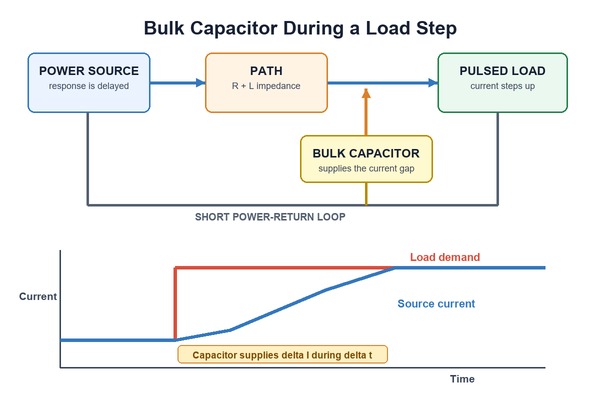
The source cannot change its delivered current at the load terminals instantly. A regulator has finite control-loop bandwidth. Cables, connectors, fuses, planes, and vias add resistance and inductance. During the response gap, the capacitor supplies the difference between load demand and source current. When a load suddenly decreases or returns energy, the capacitor absorbs charge and slows the rail rise.

Its practical duties can include:

  • Bridging a rising load: The capacitor supplies current until the regulator or remote source catches up. The design target is the minimum voltage observed at the protected load.
  • Absorbing a falling or regenerative load: Stored or returned energy charges the capacitor. The maximum rail voltage, clamp strategy, and discharge path determine whether capacitance alone is sufficient.
  • Reducing low-frequency ripple: The capacitor delivers charge between source-current pulses. The pulse interval and allowed ripple set the required effective capacitance.
  • Isolating a board from a high-impedance feed: A local reservoir reduces the immediate current demanded through long leads or connectors.

The term bulk capacitor describes a circuit role rather than a specific component family. The correct part is the one that can supply or absorb the required charge at the rail voltage, temperature, ripple current, and service-life conditions of the product. That part may be an aluminum electrolytic, polymer, tantalum, ceramic, film capacitor, or a coordinated bank of several technologies.

What Is the Difference Between a Bulk Capacitor and a Decoupling Capacitor?

A bulk capacitor and a decoupling capacitor both control rail impedance, but they solve different parts of the same power-distribution problem. The useful distinction is the current event each capacitor must support and the length of its current loop.

Comparison Bulk capacitor Decoupling capacitor
Primary job Supplies or absorbs charge during a longer or higher-energy rail event Supplies the fastest current edge at an IC power pin
Typical event Regulator response delay, cable-fed load step, motor startup, radio burst, or rectified ripple Logic switching, clock edges, and high-frequency IC current pulses
Placement At a board input, regulator, load cluster, or other point where stored energy is needed Immediately beside the relevant power and ground pins
Current loop May include a rail segment, connector, regulator, or load group Kept as short and low-inductance as the layout allows
Common technologies Electrolytic, polymer, tantalum, ceramic, film, or a mixed bank Usually small, low-inductance ceramic capacitors
Selection basis Charge demand, support time, allowed rail movement, ESR, ripple current, and source response Target impedance, edge rate, package inductance, pin location, and IC guidance
Can it replace the other? No. Stored energy cannot overcome a long loop’s inductance during the fastest edge No. A small local capacitor may not store enough energy for a longer load event

There is no universal capacitance value that separates bulk from decoupling. A 22 µF ceramic may act as bulk capacitance on one device rail, while a board input may need several thousand microfarads. Many designs also use intermediate capacitance between the two. Review the complete impedance network because parallel values can create resonant peaks, and a very low-ESR bank can affect regulator stability.

What Parameters Do You Need Before Calculating Bulk Capacitance?

The calculation needs a defined electrical event and a voltage budget. Without those inputs, the result is only a copied rule of thumb and cannot show whether the protected rail stays within its operating limits.

  • Rail voltage and permitted range: Record the nominal voltage, minimum acceptable voltage, maximum acceptable voltage, source tolerance, and any startup or regenerative peak. Separate the total allowed movement from the portion available for capacitor discharge.
  • Current change: Record the initial load current, final load current, and the current the source can deliver during the event. The capacitor supports the shortfall, which may be smaller than the final steady-state load.
  • Support time: Determine how long the current shortfall lasts before the regulator, upstream converter, battery, or remote supply responds. Use control-loop data, a load-step measurement, simulation, or a conservative system requirement. Switching frequency is not automatically the response time.
  • Load slew rate and waveform: A 1 A change in 10 ns and the same change in 10 ms need different impedance control. Capture pulse duration, repetition rate, duty cycle, and whether the current ramps or steps.
  • Source and distribution impedance: Include the cable, connector, fuse, copper path, vias, and protection elements between the source, capacitor, and load. Their resistance and inductance consume part of the voltage budget.
  • Operating corners: Identify minimum input voltage, maximum load, cold-start ESR, hot-operation lifetime, tolerance, aging, and the physical configuration that produces the worst rail response.
  • Energy direction: A rising load causes droop. Motor braking, solenoid release, load shedding, or cable disconnection can cause overshoot. Both directions may govern the same capacitor bank.

The voltage limit must be defined at the point where failure occurs. A stable waveform at the regulator does not prove that the processor pins, motor-driver supply, radio module, or board connector stays in range. State the measurement node before calculating the capacitor.

How Do You Calculate the Required Bulk Capacitor Value?

Calculate the charge that must be supplied during the interval before the source responds, then divide it by the voltage movement allocated to capacitor discharge. For an approximately constant current shortfall, the first estimate is:

Bulk capacitor, diagram showing a capacitor supplying the current gap during a load step before the power source responds

C ≥ ΔI × Δt ÷ ΔVC

Here, ΔI is the current the capacitor must provide, Δt is the support interval, and ΔVC is the capacitive portion of the allowable rail change. If the load or source current ramps, calculate the area between the two current waveforms instead:

C ≥ ∫(Iload − Isource)dt ÷ ΔVC

Before using either expression, subtract the immediate resistive drop from the total voltage budget:

ΔVESR ≈ ΔI × ESR

PCB resistance and fast inductive spikes may require additional allowance. Texas Instruments’ load-transient capacitance guidance also treats the charge equation as an estimate that must account for converter response and non-ideal capacitor behavior.

A worked load-step example

Assume a 5 V rail experiences a 1.5 A load increase. The source needs 300 µs to supply the additional current, and the protected circuit permits a 0.25 V dip. The proposed capacitor and interconnect have 30 mΩ of effective series resistance during the event.

  1. Calculate the ESR step: 1.5 A × 0.030 Ω = 0.045 V.
  2. Find the remaining capacitive budget: 0.25 V − 0.045 V = 0.205 V.
  3. Calculate effective capacitance: 1.5 A × 300 µs ÷ 0.205 V = 0.00220 F, or approximately 2,200 µF.
  4. Convert the effective requirement into a part requirement: Add margin for tolerance, temperature, voltage dependence, aging, and source-response uncertainty. A nominal 2,200 µF part is not automatically sufficient.
  5. Check the complete rail: Verify regulator stability, startup, inrush, ripple current, overshoot, and the measured load-step response.

This is a hypothetical screening calculation, not a universal value. If the source current rises during the 300 µs interval, integrating the actual current difference can reduce the estimate. If the load edge is very fast, local ceramic capacitors are still required to control the leading edge while the bulk bank supports the longer pulse.

How Do ESR, ESL, Ripple Current, and DC Bias Affect the Actual Value?

They determine whether the nominal capacitance can control the real waveform without overheating or destabilizing the circuit. The calculated value is an effective in-circuit requirement; it must survive the electrical and environmental conditions of the finished assembly.

  • ESR creates an immediate voltage step and heat: The current change multiplied by ESR appears before appreciable capacitive discharge. Lower ESR can reduce droop, but some regulators require a defined ESR range, and a low-loss bank connected through an inductive feed can ring.
  • ESL limits the fastest response: Package geometry, leads, pads, vias, and trace length add inductance. A large capacitor located behind a narrow or long path may provide little help during the first part of a fast edge.
  • Ripple current raises core temperature: AC current flowing through ESR produces heat. Compare the expected RMS ripple, frequency, ambient temperature, and cooling conditions with the manufacturer’s rating and lifetime model.
  • DC bias can reduce ceramic capacitance: High-capacitance Class 2 MLCCs may retain only a portion of their labeled value at operating voltage. Murata’s DC-bias explanation shows why the part-specific bias curve belongs in the sizing calculation.
  • Tolerance, temperature, and aging reduce the guaranteed minimum: Use the worst credible combination rather than adding nominal values. Parallel parts also may not share ripple equally when ESR, temperature, or interconnect impedance differs.
  • Voltage stress and polarity set safe operating limits: Include line variation, startup overshoot, regenerative rise, ripple peaks, derating, and reverse-voltage exposure.

Aluminum electrolytic lifetime is especially sensitive to core temperature. Nearby power semiconductors, restricted airflow, and ripple heating can shorten service life even when room-temperature measurements look acceptable. Nichicon’s application guidance for aluminum electrolytic capacitors requires operation within the applicable voltage, ripple-current, temperature, polarity, and lifetime limits.

How Do You Choose the Right Type of Bulk Capacitor?

Choose the technology by matching its effective capacitance, impedance, ripple capability, voltage behavior, lifetime, package, and failure risks to the event defined earlier. The following options solve different constraints:

  • Aluminum electrolytic for high capacitance at board inputs: It is often practical when the rail needs hundreds or thousands of microfarads at moderate cost. Check ripple-current rating, ESR at the coldest operating temperature, expected life at the measured case temperature, polarity, and vent clearance. Its larger size and finite service life may limit compact or high-vibration products.
  • Aluminum polymer for low ESR and high ripple current: It can reduce the immediate ESR-related voltage step on compact low-voltage rails. Confirm rated voltage, surge tolerance, leakage, regulator stability, and the manufacturer’s ripple conditions. The tradeoff is usually higher cost and a narrower voltage range than many electrolytics.
  • Tantalum or tantalum polymer for compact, stable capacitance: These parts can fit space-constrained rails that need predictable capacitance. Review voltage derating, surge and inrush behavior, failure mode, and protection requirements before approval.
  • High-capacitance MLCCs for a low-inductance response: Ceramic banks help when low ESR and ESL matter, but the part-specific DC-bias curve may leave far less capacitance than the label suggests. Also check temperature class, board-flex cracking risk, acoustic behavior, and the current shared by each package.
  • Film capacitors for high voltage, pulse current, or low loss: Film technology is useful when repetitive pulses, low dielectric loss, or voltage stress dominate the design. Confirm physical volume, termination-current capability, mounting, and vibration support because the required package may be large.
  • A hybrid bank when one technology cannot cover the full impedance range: Combining a bulk electrolytic or polymer part with local ceramics can divide the energy and high-frequency duties. Model or measure the network so that anti-resonance and regulator stability are controlled rather than assuming more parallel values are always better.

After selecting the technology, lock exact manufacturer part numbers or reviewed alternates in the BOM. An unreviewed substitution can change capacitance under bias, ESR, ripple rating, lifetime, voltage margin, or package geometry even when the printed µF value is unchanged.

Where Should a Bulk Capacitor Be Placed on a PCB?

Place it where it closes the current loop responsible for the rail disturbance. Distance alone is an incomplete rule: the supply path, return path, switching device, source of the transient, and measurement point determine whether the capacitor is electrically close.

  • At the board power entry: Put the reservoir after the connector, fuse, or protection stage when the board must ride through impedance in the external feed. Confirm that the source and protection path tolerate charging current.
  • At a regulator input: Keep the high-current input loop short. A distant board-level reservoir cannot replace the local input capacitor required by the regulator data sheet.
  • At a regulator output: Follow the permitted capacitance and ESR range, then connect the bank through short, wide power and return paths. Sense lines should observe the intended load point.
  • Near a pulsed or regenerative load: Place local energy storage at the motor driver, solenoid driver, radio power amplifier, or other pulsed load when interconnect impedance would otherwise dominate the event.
  • Across a distributed rail: Several reservoirs near separate load clusters can outperform one distant bank. Each bank still needs a defined role and an interaction check with the rest of the power-distribution network.

Route power and return as a pair. Avoid a narrow copper neck between the capacitor and load, and use enough vias for the transient current. For polarized or tall parts, make polarity clear, provide vent and mechanical clearance, keep heat sources away, and review shock or vibration when the product environment requires it.

How Does Bulk Capacitor Sizing Change for Different Applications?

The governing equation changes with the source waveform and energy path. The same charge relationship applies, but the current interval, voltage boundary, ripple spectrum, and failure consequence differ by application.

  • Point-of-load regulator output: The regulator’s control-loop response defines the support interval. Both minimum and maximum output capacitance, ESR, load-step droop, and recovery behavior must remain inside the regulator’s stability requirements.
  • Board input fed through a cable: Cable and connector impedance may make the local bank supply a pulse before the remote source responds. Cable length, source current limit, hot-plug behavior, inrush, and input-filter damping become part of the calculation.
  • Motor or solenoid driver: Startup current can create droop, while braking or current interruption can return energy and create overshoot. Calculate both directions and determine whether a clamp, brake resistor, transient suppressor, or bidirectional source is also required.
  • Rectified AC reservoir: The capacitor supplies the load between charging peaks. Use the rectified ripple interval, load waveform, line frequency, conduction angle, ripple-current rating, and safety requirements rather than a regulator load-step time.
  • Radio, LED, or pulsed load: Pulse current, pulse width, repetition rate, and permitted modulation of the rail drive the required charge. Check cumulative ripple heating as well as the voltage movement during one pulse.
  • Battery-powered product: Battery impedance, protection FETs, wiring, state of charge, and cold-temperature behavior may dominate the source path. Extra capacitance can help a short pulse but may increase connector spark, protection stress, or startup delay.

For every case, calculate at the node that must stay inside its voltage limit. A capacitor value derived for a board connector cannot automatically guarantee the voltage at a distant device rail.

What Happens If the Bulk Capacitor Is Too Large or Too Small?

Too little capacitance allows excessive droop, ripple, or overshoot; too much capacitance can create charging, stability, and stored-energy problems. The acceptable range is set by the source, regulator, protection circuit, and operating event rather than by a preference for the largest available value.

If the value is too small, the clearest warning signs are processor resets, excessive rail ripple, motor-driver undervoltage trips, regenerative overshoot, and high capacitor temperature because too few parts share the ripple current.

If the value is too large, check for excessive inrush, connector arcing, nuisance operation of a fuse or current limiter, failed startup, regulator instability, and an overly long discharge time. The extra stored energy can also increase fault stress, board area, and mechanical load.

The design therefore needs a verified capacitance range rather than a single minimum number. Confirm the lower limit with the worst load transient and effective capacitance, then confirm the upper limit against startup, inrush, stability, protection, and discharge requirements.

How Do You Verify Bulk Capacitor Performance on an Assembled PCB?

Verify the same event and limits used in the calculation. A capacitance meter or BOM check confirms a component property, but only a powered test at the correct node shows whether the assembled PCB controls droop, overshoot, ringing, and temperature.

  • Reproduce the worst credible event: Apply the specified load step, pulse train, startup sequence, line condition, or regenerative event. Record current amplitude, edge rate, duration, repetition rate, input voltage, cable configuration, and temperature.
  • Probe at the protected node: Measure power and return at the load pins or defined test points. Use a short oscilloscope ground spring or suitable differential probe so the measurement loop does not invent a spike.
  • Interpret the waveform by region: The first voltage step points to ESR and path inductance. The following slope reflects capacitance and charge removal. Later recovery reflects the source and control loop.
  • Test both current directions: Measure droop when the load rises and overshoot when it falls. For motors and inductive loads, include braking, reversal, and supply-disconnection cases.
  • Check startup and faults: Confirm that the source starts reliably, current limiting does not nuisance-trip, connectors remain within rating, and stored energy discharges as required.
  • Measure thermal stress: Record capacitor case temperature during sustained ripple at the worst ambient condition, then apply the selected part’s ripple and lifetime model.
  • Lock the verified configuration: Record part numbers, quantities, locations, board revision, firmware or load state, test setup, and acceptance limits. Re-test alternates or layout changes that affect the power loop.

Match the correction to the observed waveform. A large instantaneous step calls for lower ESR or a shorter loop. A continuing slope calls for more effective capacitance or a faster source response. Ringing calls for impedance and stability analysis. Adding capacitance without identifying the failing region can hide one symptom while creating another.

What Are the Most Common Bulk Capacitor Selection Mistakes?

The most common mistakes come from replacing a defined electrical event with one catalog number or rule of thumb. Each error can be found before production by checking the calculation inputs, part curves, layout, and powered waveform together.

  • Copying a value from another board: The other design may have a different rail, source response, current step, cable, or voltage limit. Recalculate from the present load event.
  • Using nominal capacitance as effective capacitance: Tolerance, DC bias, temperature, and aging can reduce the available value. Use the part-specific minimum at the operating point.
  • Giving the full droop budget to capacitance: ESR, copper resistance, connector resistance, and inductive spikes also move the rail. Reserve voltage margin for each known term.
  • Replacing local decoupling with one large part: A bulk capacitor cannot overcome the inductance of a long loop during the fastest current edge.
  • Ignoring the regulator’s capacitance limits: More capacitance or lower ESR can slow startup, trigger current limiting, or destabilize the loop.
  • Sizing only for load increase: Motor braking, load release, or cable disconnection can raise the rail. Check whether energy must be clamped or dissipated.
  • Checking ripple current at the wrong condition: Frequency, ambient temperature, airflow, and current sharing affect heating.
  • Placing the part beside the load but routing it through a narrow loop: Physical proximity does not compensate for shared vias, necked copper, or a remote return path.
  • Approving an alternate by µF and voltage alone: Package, ESR, ESL, ripple rating, life, surge behavior, and terminal geometry can change the result.

FAQs About Bulk Capacitors

Q1: Is a bulk capacitor always an electrolytic capacitor?

A1: No. Electrolytic capacitors are common because they provide high capacitance economically, but polymer, tantalum polymer, ceramic, film, or hybrid banks may serve the same role when their ratings suit the circuit.

Q2: Can power in watts determine the required bulk capacitance?

A2: No. Power alone does not define rail voltage, current change, support time, allowed droop, source response, ESR, pulse repetition, or returned energy. Calculate from the actual current-versus-time event and voltage limits.

Q3: Can several smaller capacitors replace one large bulk capacitor?

A3: They can when their combined effective capacitance, voltage rating, ripple capacity, ESR, ESL, layout, and lifetime satisfy the requirement. Parallel parts may lower impedance and distribute heat, but unequal paths can prevent equal current sharing and can introduce anti-resonance.

Q4: Should the bulk capacitor be placed before or after the voltage regulator?

A4: It depends on which rail event must be controlled. Input capacitance supports the switching stage and isolates source-path impedance. Output capacitance supports the regulated load and participates in loop stability. Many designs need both.

Q5: Does a bulk capacitor need a discharge resistor?

A5: Add a discharge path when stored voltage must fall within a defined time for safety, service, sequencing, or reliable restart. Balance discharge time against continuous power loss, and verify any discharge path already provided by the load or regulator.

Need help bringing a bulk capacitor design into production? Send EBest Circuit your rail voltage, load-step or ripple requirement, selected capacitor part number or approved-alternate limits, Gerber files, BOM, order quantity, delivery target, and test criteria. Our team can review the footprint, polarity, hole size, copper path, component availability, and assembly requirements together. Email sales@bestpcbs.com for a free DFM review and a quotation based on your actual board and production scope.

You may also like

Circuit Board Ground Plane: Layout Rules and Return Paths
Wednesday, September 2nd, 2026

A circuit board ground plane is a broad copper region connected to a PCB’s ground net. It provides a voltage reference and a path for returning current. Its effectiveness depends on continuity, distance from the signal layer and the connections between layers, not simply how much copper fills the screen. A layout can pass a continuity test yet still force fast return currents through a noisy detour.

Circuit board ground plane illustrated as a continuous copper layer beneath insulated signal routing

What Is a Ground Plane?

A ground plane in PCB design is the physical copper conductor assigned to the reference net, usually named GND. In PCB terminology, a GND plane or grounding plane, sometimes written groundplane, can occupy most of an outer layer or a dedicated internal ground layer. It is not automatically connected to earth: a battery-powered circuit can have a local ground reference without an earth connection.

For the question “what is a ground plane PCB?”, the distinction is straightforward: the PCB is the complete board, while its ground plane is one part of the copper structure. Schematic ground symbols specify connectivity; the manufactured copper determines the impedance of that connection.

Ground planes are also different from chassis bonds and protective-earth conductors. Those connections address enclosure, fault-current and system-level requirements. A common net name does not make their functions interchangeable.

How Does a Ground Plane Work?

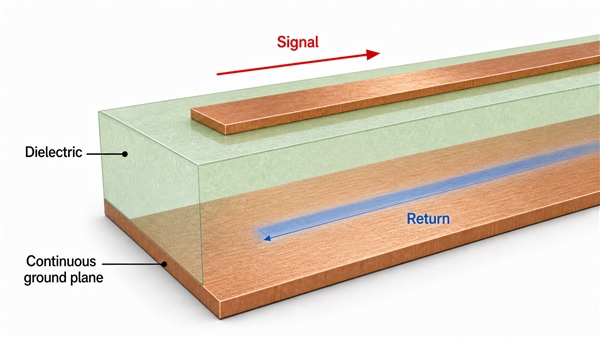
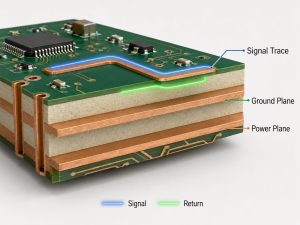
A ground plane completes the current loop between a source and its load. At low frequency, resistance strongly influences current distribution; with fast signal transitions, inductance and electromagnetic coupling become important. The high-frequency portion of the return current tends to concentrate on the nearby reference plane beneath the signal path.

The return is a distributed current, not a narrow physical track etched into the plane. A continuous reference lets that distribution follow the signal. A slot, a chain of clearance holes or a long narrow copper neck can force it elsewhere, increasing loop area and changing the local transmission-line geometry.

For example, routing a clock over an uninterrupted ground region and routing the same clock over a connector cutout are not equivalent, even if both endpoints connect to GND. Trace length alone will miss that difference. Circuit board grounding must be evaluated as a complete outgoing-and-returning path.

Conceptual signal and opposing high-frequency return directions on separate layers, not to scale

Which PCB Ground Plane Rules Matter Most?

The most useful PCB ground plane rules protect a continuous reference under critical routes and control where noisy currents travel. A large copper percentage is not a substitute for these checks.

  • Choose the stack-up before routing. Identify the reference conductor for each signal layer, including the layer after every transition.
  • Keep critical routes over continuous copper. Check slots, antipads, plane edges and narrow connections, not only obvious split lines.
  • Place by current flow. Keep switching loops and digital interfaces away from low-level analog input paths.
  • Provide local return transitions. Connect same-net ground references near signal-layer changes where the return must change planes.
  • Preserve clearances. Copper fill must not violate electrical spacing, board-edge or isolation requirements.
  • Inspect the filled result. Refill copper after layout changes and review the manufacturing output, not just the polygon boundary.

PCB ground plane design should also account for edge rate. A low clock frequency does not mean its digital edges are slow. Plane spacing, trace geometry and the device’s transition times together determine whether a seemingly short connection needs transmission-line treatment.

How Should a 2 Layer PCB Ground Plane Be Arranged?

A 2 layer PCB ground plane is usually easiest to preserve when most components and signal routing remain on one side and the other side stays predominantly ground. Every trace inserted into that ground side consumes some of the available return path.

On a 2 layer circuit board, a short crossover may be manageable, but a row of parallel bottom-side traces can divide the copper into long strips. Move components or reroute the upper layer before accepting a ground region connected only by a thin neck. Inspect the copper underneath each fast or sensitive route from source to load.

A 2 layer PCB board is not automatically unsuitable for fast signals, but it provides fewer routing options for maintaining a close, continuous reference. A thick two-layer dielectric can also make practical controlled-impedance routing more difficult. Compare the proposed geometry with a manufacturable four-layer stack before locking the board thickness.

We manufacture FR4 printed circuit boards for these constructions. Layer count, dielectric spacing and copper thickness should be considered together; adding a copper pour after routing cannot correct every return-path problem.

What Changes with a 4 Layer PCB Ground Plane?

A 4 layer PCB ground plane can provide a dedicated internal reference that routing does not repeatedly interrupt. The benefit comes from the actual layer arrangement, not the number four itself.

Illustrative stack-up Useful feature Design limitation
Signal / dielectric / GND Simple two-layer construction Ground-side routing and large dielectric spacing can constrain performance
Signal / GND / power / signal Dedicated ground and power distribution Bottom routing often references the power plane; splits and reference transitions need attention
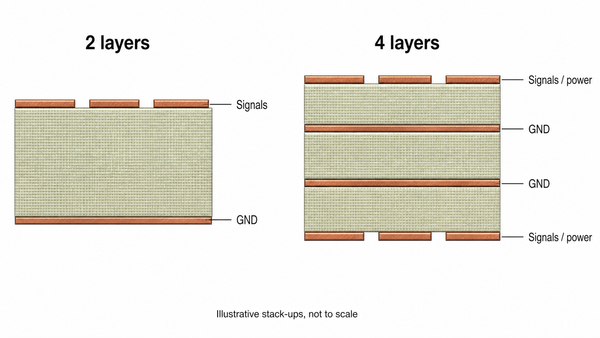
Signal-power routing / GND / GND / signal-power routing Both outside signal layers can have adjacent ground references Power must be distributed in suitable traces or pours; current capacity still needs checking

PCB power and ground planes serve different nets. A PCB power plane can act as an AC reference in a suitable design, but return transfer to ground depends on the power-distribution network, including decoupling and plane coupling. Do not assume a signal via automatically provides that transfer.

For multilayer circuit board planes, specify the copper order and actual dielectric thicknesses. Two boards with the same total thickness can have very different trace-to-reference spacing. The drawing below illustrates two possible arrangements, not a production stack-up specification.

Two-layer and four-layer examples showing signal conductors separated from continuous ground copper by dielectric

Should a PCB Ground Plane Be on the Top and Bottom?

Using a PCB ground plane top and bottom can be useful when both copper regions connect to the same ground net and support the intended return paths. Two pours connected only at a remote point do not necessarily behave as one low-impedance reference at high frequency.

Place ground connections where currents actually change layers, near appropriate connector returns and where local copper would otherwise be poorly connected. Avoid leaving disconnected copper islands. Revisit fill clearance and thermal-relief settings if the pour looks connected visually but the final geometry contains only weak connections.

More copper is not always appropriate. Antenna keepouts, isolation barriers and some sensitive high-impedance or switching nodes require deliberately controlled copper placement. Preserve those requirements instead of filling every unused area by default.

Ground Plane vs Ground Pour: What Is the Difference?

A ground pour describes a CAD-generated copper area; a ground plane describes the electrical reference structure it is intended to provide. A ground pour can form an effective plane, but its name does not guarantee continuity.

In PCB ground plane layout, evaluate the final copper rather than the rectangle used to define it. Track clearances, pad clearances and via antipads remove copper from that rectangle. A nearly full layer can still have an obstructed return path beneath one critical signal.

Solid fill generally offers more continuous conductive area than a hatched region. Hatching may be required in specific flexible constructions or for mechanical reasons, but it changes the return geometry. It should be an intentional construction choice, not a cosmetic setting applied to every design.

Where Should Ground Stitching Vias Be Placed?

PCB ground plane stitching is most useful where it connects return structures that otherwise have an inconvenient path between them. Place vias according to the signal transition, connector structure and frequency-dependent field behavior, not a universal spacing rule.

If a signal changes from a layer referenced to one GND plane to a layer referenced to another GND plane, nearby ground vias can shorten the return transition. A signal via is not itself a ground connection. If the reference changes between power and ground, a same-net ground stitching via alone does not solve the problem.

Dense packages introduce a second issue: closely spaced antipads can leave little copper between holes. Adding more ground vias without examining those openings can make the reference geometry worse. Check drill and copper clearances as well as the net connections.

Our HDI boards support compact routing structures where this interaction matters. Blind and buried via choices affect which layers can actually be connected; use the approved layer span rather than assuming every via reaches every ground plane. Our PCB via types guide explains those construction differences.

Should Signal Ground and Power Ground Be Split?

Signal ground and power ground should be arranged to prevent large or rapidly changing currents from corrupting sensitive references. They do not automatically require a physical split in the plane.

On many mixed-signal boards, sensible placement over a continuous plane keeps local return loops separated without forcing signals across a gap. AGND, DGND and power GND labels must still be interpreted using the actual IC documentation. They describe circuit functions; they are not a universal instruction to cut the board’s copper into separate regions.

A deliberate split may be necessary for a particular architecture. In that case, define how signals cross the boundary and how their returns close. True galvanic-isolation barriers are different: do not add stitching vias or casual copper bridges across them to improve signal return.

A PCB ground loop problem also needs a system view. Multiple cable and chassis connections can create unwanted current paths, while several local stitching vias between the same ground planes can be beneficial. Removing vias simply because they form a geometrical loop is not a reliable noise cure.

How Do You Create and Check Ground Copper in CAD?

Assign the copper region to the correct GND net, configure its clearances and pad connections, refill it, then inspect the exported layers. A colored polygon with the wrong net assignment is not a working ground plane.

Ground Plane PCB KiCad Workflow

For a KiCad ground plane, use a copper zone on the intended layer, set its net and review clearance, thermal and island-removal settings. Refill after editing and run the design-rule checker. Inspect isolated regions and narrow copper necks in addition to reported violations.

Ground Plane EasyEDA Workflow

The ground plane EasyEDA workflow follows the same electrical checks: choose the copper-area layer and GND net, review fill and pad-connection settings, and rebuild the copper. Command labels can differ by editor version. Confirm the final Gerber copper matches the intended return path before treating the preview as complete.

A rule checker verifies configured constraints. It does not by itself prove that a fast return current has a favorable path or that an isolated island is harmless. Net highlighting and a layer-by-layer review remain necessary.

How Can You Verify a Circuit Board Ground Plane?

Verify both connectivity and behavior. Electrical testing can find opens or shorts, while signal-integrity and EMC checks address problems that a DC continuity measurement cannot reveal.

Check What it can reveal What it does not prove
Netlist and filled-layer review Wrong nets, missing joins, copper slots and isolated regions Actual high-frequency performance
Unpowered continuity and resistance tests Open connections or unintended shorts Low inductance or correct impedance
Stack-up and impedance review Reference spacing and geometry consistency Every return transition is well designed
Waveform and noise measurements Ringing, ground-reference movement and load-related interference Regulatory EMC compliance
EMC evaluation System emissions and susceptibility under defined conditions Reliability under every operating condition

Disconnect power and discharge stored energy before continuity checks. For powered low-voltage measurements, use an appropriate short probe reference; a long ground lead can add misleading ringing. A grounded oscilloscope must not be attached casually to a floating or hazardous node. Use measurement equipment and isolation methods rated for the actual circuit.

Manufacturing review also covers copper balance, thermal connections and the clearance left between holes. These checks complement circuit validation rather than replacing it.

Close-up illustration of PCB ground copper, isolated signal pads and plated vias for layout review

Ground Plane Questions

1. Can a circuit board ground wire replace a plane?

A circuit board ground wire can provide a return connection in a suitable low-frequency or low-current circuit. It does not reproduce the broad, closely coupled reference of a plane for fast signals. Evaluate wire length, loop geometry and transient current, not just DC resistance.

2. Does a larger ground area always reduce noise?

No. A large area can still have narrow necks, unsuitable current sharing or poor connections between layers. Placement, continuity and the return-loop geometry matter more than copper coverage alone.

3. How is a ground plane antenna different?

A ground plane antenna intentionally uses a conductive reference as part of its radiating structure. An antenna ground plane may function as a counterpoise rather than simply as a shield. Design the ground plane for antenna operation together with the feed geometry and keepout. Flooding copper beneath every antenna is not a universal improvement.

For our RF printed circuit boards, material properties, reference spacing and copper geometry must be reviewed together. Ground copper useful beside an RF feed may still be prohibited in the antenna’s keepout region.

4. Do differential pairs need a reference plane?

Differential routing does not eliminate reference-plane considerations. Coupling between the pair, coupling to the plane, common-mode behavior and asymmetry all matter. Avoid routing the pair across an arbitrary reference gap merely because the signals are differential.

5. Can thermal reliefs be used on ground connections?

Yes, when their geometry meets electrical and assembly requirements. Thermal spokes can improve solderability, but their width and count also affect current capacity and impedance. High-current terminals and high-frequency connections may require a different attachment strategy.

Ground Plane Fabrication Support

We review manufacturability together with the specified stack-up and copper geometry. At EBest Circuit (Best Technology), our FR4 capability extends to up to 32 layers, and our HDI capability includes line/space down to 2/2 mil, subject to materials, board dimensions, stack-up and engineering review. These are capability limits, not default dimensions for every ground-plane design.

Our PCB manufacturing capabilities support construction planning, but finer traces and more layers do not guarantee a better return path. The finished board must preserve the reference geometry specified by the circuit design, and the assembled product still needs its appropriate electrical and EMC validation.

Conclusion

A useful circuit board ground plane is continuous where signals need it, connected where return currents change layers, and kept clear where isolation or antenna requirements demand it. Review the filled copper beneath critical routes, not just the GND net name. For stack-up and fabrication support, contact our team at sales@bestpcbs.com.

You may also like

Transistor Pinout Guide for PCB Layout and PCBA Assembly
Wednesday, May 13th, 2026

A transistor pinout shows how the pins of a transistor are arranged in its physical package. For a BJT transistor, these pins are usually Emitter, Base, and Collector. For PCB layout and PCBA assembly, this small detail is very important. It affects the schematic, footprint, SMT placement, BOM review, and final circuit performance.

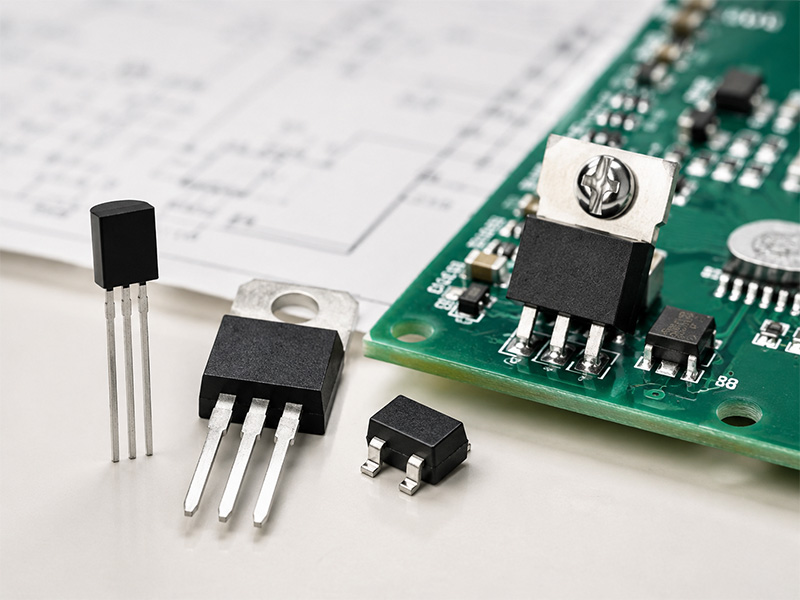
At first glance, a transistor looks simple. It may only have three pins. However, the same transistor family can come in several packages, such as TO-92, SOT-23, TO-220, SOT-223, or DFN. In addition, different manufacturers may use different pin arrangements for similar-looking parts.

Therefore, engineers should confirm the transistor pinout before PCB layout starts. They should also check it again before SMT assembly. This helps reduce footprint errors, wrong part orientation, and avoidable production issues.

This guide explains transistor pinout from a PCB and PCBA point of view. It is written for engineers, hardware teams, purchasing teams, and product companies that need reliable PCB manufacturing and assembly.

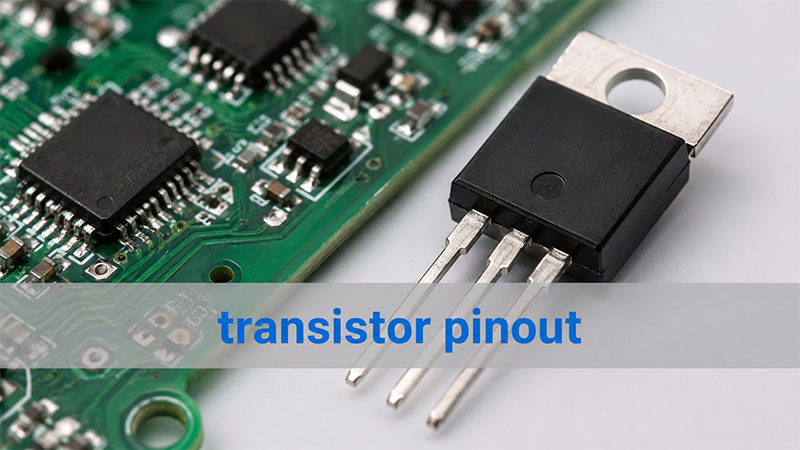
transistor pinout

What Is a Transistor Pinout?

A transistor pinout is the physical order of the transistor pins. It tells you which lead or pad connects to each internal function of the device.

For a BJT transistor, the three main pins are:

Pin NameShort NameMain Function
EmitterEWorks as one side of the main current path
BaseBControls the transistor switching or amplification
CollectorCConnects to the load or output side in many circuits

For PCB design, the transistor pinout must match three things:

  • The schematic symbol
  • The PCB footprint
  • The actual component package

If these three parts match, the circuit has a much better chance of working correctly after assembly. However, if one part is wrong, the finished PCB may fail during testing.

For example, a TO-92 transistor may look the same as another TO-92 transistor. Even so, the pin order may be different. One part may use E-B-C order, while another may use C-B-E order. Because of this, engineers should not rely only on the package shape.

Instead, the safest method is to check the official datasheet. Then, compare the datasheet pinout with the PCB library footprint.

Why Does Transistor Pinout Matter in PCB Layout and PCBA Assembly?

Transistor pinout matters because it affects how the real part connects to the circuit. In a PCB file, the footprint may look correct. During SMT assembly, the component may also be placed neatly. However, the circuit can still fail if the footprint pin mapping is wrong.

In PCB layout, transistor pinout affects routing, pad numbering, copper layout, and test point planning. In PCBA assembly, it affects pick-and-place rotation, AOI inspection, and functional testing.

For instance, an SOT-23 transistor has a very small body and three pads. The package looks simple. Yet the electrical pin order is not always the same for every part. As a result, one wrong footprint can cause many assembled boards to fail.

A correct transistor pinout helps avoid:

  • Wrong PCB footprint selection
  • Incorrect schematic-to-layout mapping
  • SMT orientation errors
  • NPN and PNP part mix-ups
  • Wrong alternative transistor selection
  • Failed functional testing after assembly
  • Extra rework during pilot production

Therefore, pinout checking should be part of the normal DFM review process. It is a small step, but it helps protect the full PCB production flow.

For EBest Circuit projects, this type of check connects directly with PCB fabrication, SMT assembly, BOM review, DFM support, and turnkey PCBA production.

What Do Emitter, Base, and Collector Mean in a BJT Transistor Pinout?

In a BJT transistor pinout, the three pins are Emitter, Base, and Collector. Each pin has a different role in the circuit.

BJT PinShort NameWhat It DoesPCB Design Note
EmitterEConnects to one side of the current pathMust match the expected current direction
BaseBControls the transistorUsually needs a proper resistor
CollectorCOften connects to the load sideRouting should follow the circuit design

The Base is the control pin. A small signal at the Base can control a larger current between the Collector and Emitter. Because of this, BJT transistors are widely used for switching and amplification.

However, the physical pin order can be different from what beginners expect. A schematic symbol may show the Base in the middle. Still, the actual transistor package may not place the Base on the middle lead.

For that reason, engineers should always check the package drawing. They should also confirm the view direction. Some datasheets show the front view, while others show the bottom view. This detail is easy to miss during library creation.

In short, knowing Emitter, Base, and Collector is only the first step. The more important step is making sure these pins are mapped correctly to the PCB pads.

How to Determine Transistor Pinout Before PCB Design?

The best way to determine transistor pinout before PCB design is to check the official datasheet. Then, compare the datasheet with the schematic symbol, PCB footprint, and BOM part number.

A simple engineering workflow is shown below:

StepWhat to CheckWhy It Matters
1Full part numberSimilar part names may have different packages
2Manufacturer datasheetIt gives the most reliable pinout data
3Package drawingPin order depends on the viewing direction
4Schematic symbolPin names must match the real transistor
5PCB footprintPad numbers must connect to the correct pins
6BOM alternativesSubstitute parts may use different pinouts
7SMT orientationPlacement data must match the package direction

This process is useful for both through-hole and SMD transistors. However, it becomes even more important for SMT assembly. Small packages leave little room for visual correction after placement.

Also, engineers should check the complete ordering code. A short part name may not be enough. For example, one transistor family may include TO-92, SOT-23, and metal-can versions. Although the electrical function may be similar, the package pinout can be different.

Before releasing Gerber files, the design team should review the pinout together with the footprint. In addition, the assembly team should check the pick-and-place file before SMT production.

This habit saves time. More importantly, it helps the project move smoothly from prototype to batch production.

NPN Transistor Pinout vs PNP Transistor Pinout: What Should Engineers Check?

NPN and PNP transistors both use Emitter, Base, and Collector pins. However, their current direction and circuit polarity are different. Therefore, engineers must check both the transistor type and the physical pinout.

ItemNPN TransistorPNP Transistor
Symbol arrowPoints outwardPoints inward
Common useLow-side switchingHigh-side switching
Control styleTurns on with positive base driveTurns on with negative base drive
PCB check pointCollector load path and base resistorEmitter supply path and polarity
Assembly concernMay look similar to PNP partsRequires clear BOM control

In PCB projects, an NPN transistor and a PNP transistor may use the same package shape. For example, both can be supplied in SOT-23 or TO-92 packages. As a result, the assembly line may not easily tell the difference by shape alone.

Because of this, BOM accuracy is very important. The approved manufacturer part number should be clear. The reference designator should also match the correct transistor type.

In addition, substitute parts should be reviewed carefully. A replacement transistor must match the package, pinout, polarity, voltage rating, current rating, and power rating.

For PCBA assembly, clear documentation is helpful. Assembly drawings, centroid data, and BOM files should all point to the same part direction. This makes SMT production more stable and easier to inspect.

How Do SMD Transistor Pinouts Affect SMT Placement?

SMD transistor pinouts affect SMT placement because the part is mounted by pad position and rotation angle. If the footprint is wrong, the SMT machine can still place the part correctly from a mechanical view. However, the circuit connection may still be wrong.

SOT-23 is one of the most common SMD transistor packages. It is small, easy to place, and widely used in compact PCB designs. Even so, SOT-23 pinouts are not universal. Different devices may use different pin mapping in the same package outline.

SMD PackageCommon UseSMT Placement Note
SOT-23Small-signal switchingCheck Pin 1 and footprint mapping
SOT-223Medium-power applicationsReview copper area and heat path
SOT-89Power and regulator-style circuitsCheck pad size and thermal design
DFN / QFN-style packagesCompact circuit designsConfirm hidden pad and stencil design

During SMT assembly, the pick-and-place machine follows the centroid file. It places the part according to X-Y position and rotation. However, it does not know whether the electrical pinout is right.

Therefore, engineers should check several files before production:

  • Datasheet package drawing
  • CAD footprint pad numbering
  • Pick-and-place rotation
  • Assembly drawing
  • BOM manufacturer part number
  • AOI inspection reference
  • Approved vendor list

In addition, SMD transistors often have small top markings. These markings can be different between suppliers. For this reason, the production team should not rely only on the code printed on the package.

A good DFM review can catch many of these risks before PCB fabrication and SMT assembly begin.

What Is the 2N2222 Transistor Pinout and 2N2222A Pinout?

The 2N2222 transistor pinout depends on the exact package and manufacturer. The 2N2222 and 2N2222A are common NPN BJT transistors. They are often used for switching and amplification. However, their physical pinout should still be checked before PCB layout.

The 2N2222 family is available in several forms. Some versions use metal-can packages. Others use plastic through-hole packages or SMD packages. Because of this, one footprint cannot cover every version.

Part NumberTypeCommon PackagePCB Design Note
2N2222NPN BJTTO-18, TO-92, SMD variantsConfirm the package-specific pinout
2N2222ANPN BJTTO-18, TO-92, SMD variantsCheck supplier datasheet
PN2222ANPN BJTTO-92Common plastic-package version
MMBT2222ANPN BJTSOT-23Common SMT version

For PCB projects, 2N2222 is a useful example of why full part control matters. A schematic may simply list “2N2222.” Later, purchasing may source a different package version. If the PCB footprint was made for another package, the assembly may face problems.

A better practice is to define the exact manufacturer part number in the BOM. Also, the package name and footprint name should be clear. If alternatives are allowed, each alternative should be checked before approval.

This is especially important when moving from prototype to mass production. During early samples, engineers may use a through-hole part. Later, they may switch to an SMT version for volume assembly. In that case, the PCB footprint and pinout must be reviewed again.

What Are Common Transistor Pinout Examples for PCB Projects?

Common transistor examples help engineers compare package types and layout notes. However, the final design should always follow the original datasheet.

Part NumberTypeCommon PackageTypical UsePCB / PCBA Note
2N2222 / 2N2222ANPN BJTTO-18, TO-92, SOT-23 variantsSwitching and amplificationConfirm package version
2N3904NPN BJTTO-92, SOT-23 variantsLow-current switchingCommon signal transistor
2N3906PNP BJTTO-92, SOT-23 variantsComplementary switchingCheck polarity and pin mapping
BC547NPN BJTTO-92General amplificationPin order may differ from 2N series
BC557PNP BJTTO-92Low-power switchingOften paired with BC547-style circuits
S8050NPN BJTTO-92, SMD variantsLow-power switchingConfirm supplier pinout
S8550PNP BJTTO-92, SMD variantsComplementary transistorOften used with S8050
BD139NPN BJTTO-126Medium-power circuitsThermal layout should be reviewed
BD140PNP BJTTO-126Complementary power stageCheck heat path and package
TIP120NPN DarlingtonTO-220Higher-current switchingReview thermal design
MMBT3904NPN BJTSOT-23SMT signal switchingOrientation is critical
MMBT3906PNP BJTSOT-23SMT signal switchingCheck approved alternatives
MRF9120RF power transistorRF power packageRF power circuitsFollow datasheet and RF layout rules

This table is useful during early component selection. Still, it should not replace datasheet checking. Similar transistor names can have different package versions. Also, the same electrical type may be sold by several manufacturers.

For production PCB projects, it is better to build an approved component list. This list should include the part number, package, footprint, supplier, and substitute options. As a result, the design team and purchasing team can work with the same information.

In addition, PCB and PCBA teams should review transistor pinout before manufacturing. This review is useful for both prototype builds and batch orders.

What Transistor Pinout Mistakes Can Cause PCB Assembly Defects?

Transistor pinout mistakes can lead to PCB assembly defects, even when PCB fabrication and SMT placement are well controlled. Most of these issues come from wrong library data, unclear BOM information, or unverified substitute parts.

MistakePossible ResultPrevention Method
Wrong footprint selectedPads connect to the wrong pinsCompare footprint with datasheet
Generic symbol usedSymbol pins do not match the packageUse verified library mapping
Substitute part has a different pinoutCircuit may not work as plannedCheck AVL and approved alternatives
SMD orientation is wrongPart is placed at the wrong angleReview centroid file and assembly drawing
TO-92 pin order is assumedThrough-hole pins connect incorrectlyConfirm package view and lead order
NPN and PNP are mixedCircuit function changesStrengthen BOM review
Thermal design is ignoredPower device runs too hotReview copper area and heat path
RF transistor layout is treated as standardRF performance may become unstableFollow datasheet layout guidance

Fortunately, most of these problems can be found before production. The key is to review the design early.

Before PCB fabrication, engineers should check the schematic, footprint, package drawing, and BOM. Before SMT assembly, the production team should check placement direction, part marking, and assembly files. After assembly, AOI and functional testing can confirm the result.

For turnkey PCBA projects, this process is even more important. A small transistor error can affect the whole batch. Therefore, early review helps improve delivery speed and production quality.

EBest Circuit supports customers with PCB fabrication, SMT assembly, component sourcing, BOM review, DFM pre-check, testing, and turnkey electronics manufacturing. For transistor-based circuits, our engineering team can help check package selection, footprint consistency, assembly orientation, and production feasibility before batch manufacturing.

All in all, a transistor pinout may look like a small detail. However, it plays a large role in PCB layout and PCBA assembly. When the pinout is correct, the schematic, footprint, BOM, and SMT data can work together smoothly.

Before releasing a PCB design, engineers should check the official datasheet, package drawing, pin numbering, footprint mapping, and approved alternatives. In addition, they should review SMD orientation and substitute parts before assembly.

This is especially useful for SOT-23 transistors, 2N2222 variants, NPN and PNP substitutions, and production projects with BOM changes.

With careful pinout verification, electronic product teams can reduce assembly risk and move from prototype to mass production with more assurance. EBest Circuit helps customers with PCB manufacturing, SMT assembly, component sourcing, DFM review, BOM optimization, and testing, supporting a smoother path from design files to reliable assembled boards. If any questions, pls feel free to contact us at sales@bestpcbs.com.

FAQs About Transistor Pinout

1. What is a transistor pinout?

A transistor pinout shows the physical order of a transistor’s pins. For a BJT transistor, these pins are usually Emitter, Base, and Collector. In PCB layout and PCBA assembly, the pinout must match the schematic symbol, PCB footprint, and actual component package.

2. How do I determine the correct transistor pinout?

The safest way is to check the official manufacturer datasheet. Engineers should confirm the full part number, package type, pin numbering, and viewing direction. Then, they should compare this information with the schematic symbol and PCB footprint before releasing the design.

3. Are all transistors with the same package pinout the same?

No. Transistors with the same package, such as TO-92 or SOT-23, may have different pin arrangements. For example, one TO-92 transistor may use E-B-C order, while another may use C-B-E. Therefore, package shape alone is not enough for PCB design.

4. Why is transistor pinout important for PCBA assembly?

Transistor pinout affects SMT placement, solder pad mapping, BOM verification, and functional testing. If the pinout does not match the PCB footprint, the component may be assembled correctly in appearance but fail electrically. That is why pinout verification should be included in DFM review before PCB fabrication and assembly.

You may also like

What is a PCB Layout? PCB design guide
Friday, January 10th, 2025

What is a PCB Layout? PCB layout is the process of arranging and positioning electronic components on a printed circuit board in order to optimize circuit performance, improve reliability, and meet specific design requirements. A good layout can reduce signal interference, lower electromagnetic radiation, and keep size and cost under control.

What is a PCB Layout? PCB design guide

What is a PCB Layout?

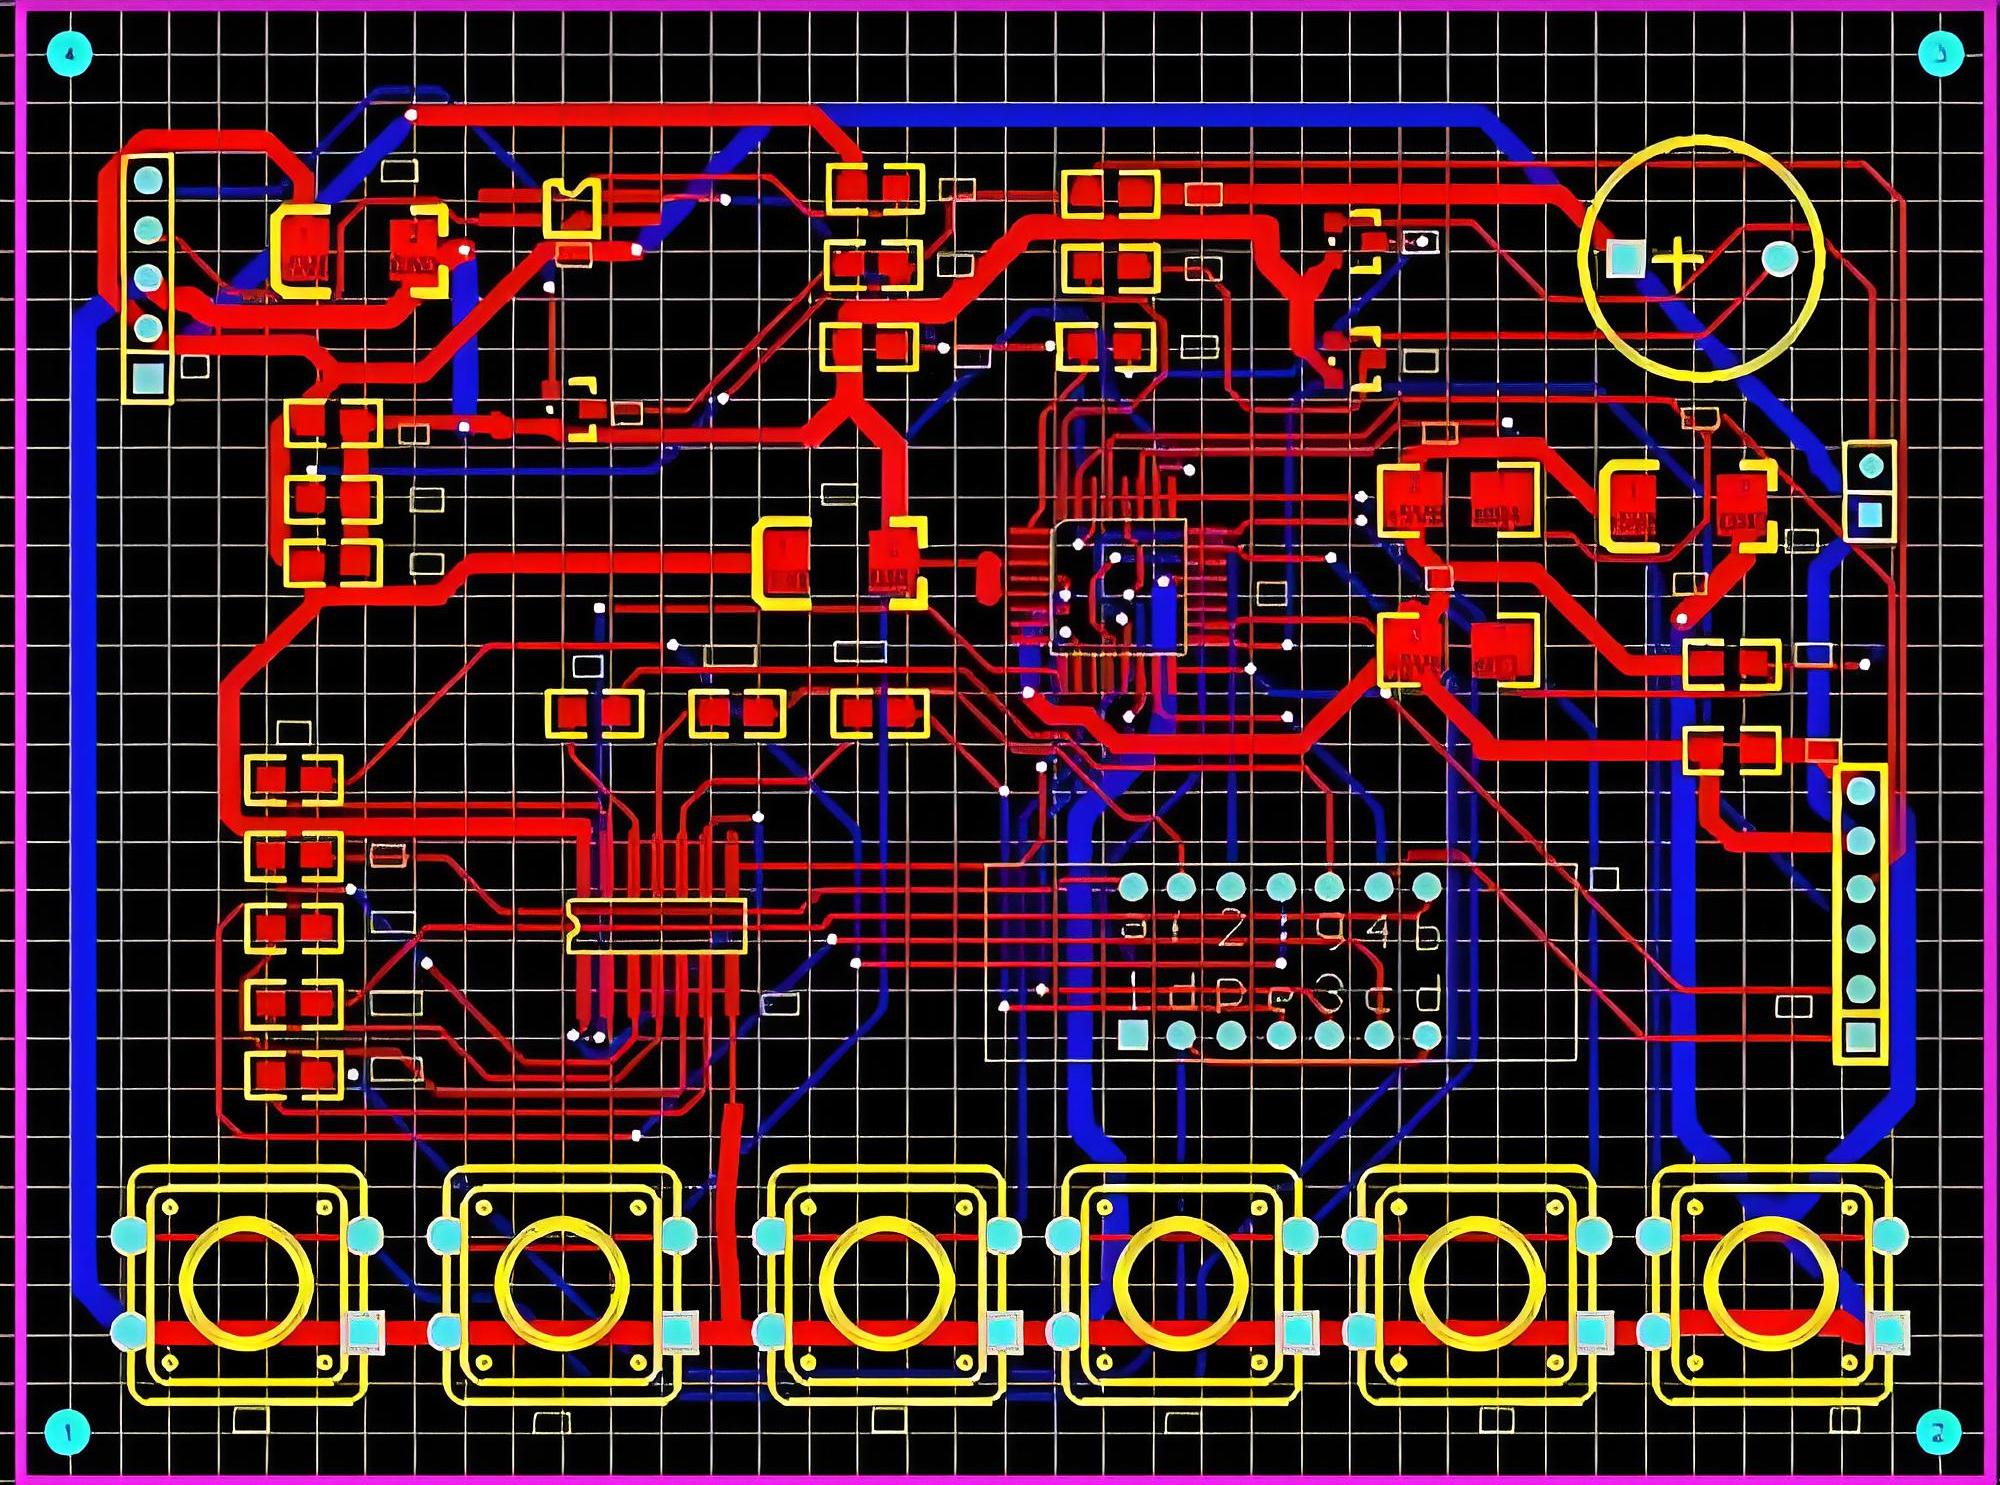
A PCB layout is the arrangement of components and the electrical connections between them on a printed circuit board. It’s essentially a map that dictates where each component goes and how electrical signals travel from one component to another.

The layout specifies the placement of parts like resistors, capacitors, integrated circuits, and connectors, as well as the routing of copper traces that carry the electrical current.

In simple terms, the PCB layout is the blueprint for building the physical circuit board. The success of the entire electronic system depends on how effectively this layout is created.. It ensures that components are connected correctly, that electrical signals travel efficiently, and that the final product meets its functional and performance goals.

How to Create a PCB Layout?

Creating a PCB layout is a process that requires attention to detail, a bit of creativity, and the right tools.

  • Start with a Schematic Design:

Before you can lay out a PCB, you need a schematic diagram. The schematic represents all the components of the circuit and how they are connected electrically. This design serves as the foundation for your PCB layout, guiding the placement of components and the routing of traces.

  • Place the Components:

This step requires careful consideration of how components should be positioned. Components should be placed logically—important parts like connectors or power supplies should be positioned in ways that make routing and assembling the board easier. High-frequency components should be positioned close to each other to reduce signal interference.

  • Route the Traces:

Traces are the electrical paths that connect components. Routing the traces involves creating paths for signals to travel between components. It’s crucial to route traces with the shortest possible path to minimize resistance and signal delay. For high-power components or sensitive signals, special care must be taken to route traces properly to avoid interference.

What is a PCB Layout? PCB design guide
  • Define Power and Ground Planes:

Power and ground planes are large areas of copper that provide a stable voltage reference for the components. These planes help reduce noise and improve the stability of the circuit. Proper grounding is especially important in high-speed or high-power circuits to avoid voltage fluctuations and interference.

  • Consider Thermal Management:

Power-hungry components generate heat, which can cause problems if not managed properly. Thermal vias, larger copper areas, and heat sinks are sometimes necessary to ensure that heat is efficiently dissipated. Placing heat-sensitive components away from high-power components can also help prevent overheating.

  • Run Design Rule Checks (DRC):

After placing the components and routing the traces, you need to check your design for errors. Design Rule Checks (DRC) are automated checks that help identify potential issues like trace width violations, inadequate spacing, or improper component placement. These checks ensure that the layout adheres to industry standards and that the board can be manufactured correctly.

  • Finalize the Layout and Export Files:

Once you’ve completed the layout and fixed any issues, the design is ready for production. The last step is to export the design file, usually in Gerber format, which is the format used to create the physical PCB.

What is the Standard PCB Format?

The most widely used format is Gerber files, which describe the layers, traces, drill holes, and components on the PCB. These files are essential for translating the layout into a physical board.

In addition to Gerber files, other essential formats used in PCB design include:

  • Bill of Materials (BOM): This document lists all the components needed for the PCB, including part numbers, quantities, and other relevant information.
  • Pick-and-Place Files: These files specify the exact locations where components need to be placed on the PCB during the assembly process.
  • Drill Files: Drill files detail the locations and sizes of holes that need to be drilled into the PCB for components or vias.

Each format plays a specific role in ensuring that the design can be accurately manufactured and assembled.

How Long Does PCB Layout Take?

The amount of time required to create a PCB layout depends on several factors, including the complexity of the design, the number of layers, and the experience of the designer.

For a simple single-layer PCB, the layout process may take only a few hours or a day. However, for more complex designs, such as multi-layer boards or designs with high-speed components, the layout can take several weeks or even months.

The complexity of the project, the need for iterative testing, and the level of optimization also influence the timeline. The more components involved and the more layers in the design, the more time it will take to finalize the layout.

Why is PCB Layout Important?

The PCB layout is crucial for several reasons:

  • Ensures Functionality: A well-designed PCB layout ensures that the electrical components interact as intended. Poor placement or incorrect routing can result in malfunctioning circuits, which could cause a device to fail entirely.
  • Minimizes Power Loss: By optimizing trace lengths and selecting appropriate trace widths, you can minimize power losses and improve the overall efficiency of the circuit.
  • Reduces Signal Interference: Properly routing traces helps reduce electromagnetic interference (EMI) and ensures signal integrity. This is particularly important in high-speed or RF (radio frequency) applications.
What is a PCB Layout? PCB design guide
  • Prevents Overheating: Effective thermal management is a key part of PCB layout. Properly placed heat sinks, thermal vias, and wide copper traces can help prevent components from overheating, which could lead to failures.
  • Improves Manufacturability: A well-designed PCB layout adheres to industry standards, which makes it easier and more cost-effective to manufacture the board. Proper layout rules ensure that the board can be produced with minimal errors and at a lower cost.
  • Supports Future Upgrades: A clear, well-documented layout makes it easier to update and improve the design in the future. Whether you need to add new features or troubleshoot existing issues, a good layout helps streamline the process.

How Do I Optimize My PCB Layout?

Optimization is key to creating an efficient, reliable PCB. Here are a few tips to help optimize your PCB layout:

  • Minimize Trace Lengths: Shorter traces reduce resistance, noise, and delay. Try to keep traces as direct as possible, especially for high-frequency or high-power components.
  • Use Wider Traces for High-Current Components: For components that draw significant power, use wider traces or dedicated bus bars to prevent overheating and power loss.
  • Avoid Trace Crossovers: Crossing traces can increase complexity and lead to errors. Try to avoid unnecessary crossovers by carefully planning the component placement.
  • Group Related Components: Group components that work together close to each other to minimize the need for long interconnections. This makes routing easier and improves signal quality.
  • Use Ground and Power Planes: A solid ground and power plane ensures stable voltage levels and reduces noise. This is particularly important in high-speed designs.
  • Check for Design Rule Violations: Always use automated design rule checks to ensure that your layout meets industry standards and manufacturing requirements. These checks help avoid errors that could complicate production.
  • Consider Thermal Management: Pay attention to heat-sensitive components and their proximity to power-hungry components. Include thermal vias or large copper areas to dissipate heat effectively.

What Are the Rules for PCB Design?

When designing a PCB layout, following certain rules is essential for creating a functional and manufacturable board. Some important PCB layout rules include:

  • Trace Width and Spacing: Ensure that traces are wide enough to carry the current they will handle and that there is enough space between traces to prevent short circuits.
  • Component Placement: Components should be placed in an organized manner, with clear signal paths and minimal trace lengths. High-speed components should be placed near each other to reduce signal degradation.
What is a PCB Layout? PCB design guide
  • Signal Integrity: Keep high-speed signal traces as short as possible and avoid running them parallel to power traces, as this can lead to noise or interference.
  • Thermal Management: Ensure that heat-sensitive components are placed away from power components and that thermal vias or heatsinks are included as needed.
  • Ground Planes: Always include a solid ground plane to reduce noise and provide a stable reference for the circuit.

What is the Difference Between PCB Layout and Design?

Although the terms “PCB layout” and “PCB design” are often used interchangeably, they actually refer to two different stages of the PCB creation process.

PCB Design refers to the overall planning stage, where the schematic is created, components are selected, and the overall functionality of the circuit is planned.

PCB Layout focuses on the physical arrangement of components and routing of traces. It’s about creating the blueprint.

In conclusion, a well-designed PCB layout is essential for the successful operation of any electronic circuit. It ensures efficient signal flow, minimizes power loss, and supports the overall reliability of the device. If you have any PCB design layout needs, please contact us via sales@bestpcbs.com to get the best solution.

You may also like