PCB manufacturing PCB manufacturing
Home > Blog

PCB Thermocouple Placement for Reflow Profiling and Temperature Measurement

September 17th, 2026

A PCB thermocouple records how hot a specific point on an assembly gets during reflow and how long it stays there. Place sensors where a joint may heat too slowly or a component may get too hot, then secure them so the readings reflect the assembly rather than the attachment. The profile must show that critical joints receive enough heat without exceeding the monitored component limits.
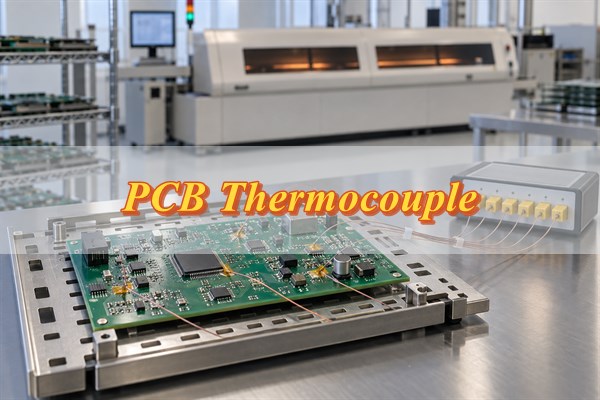
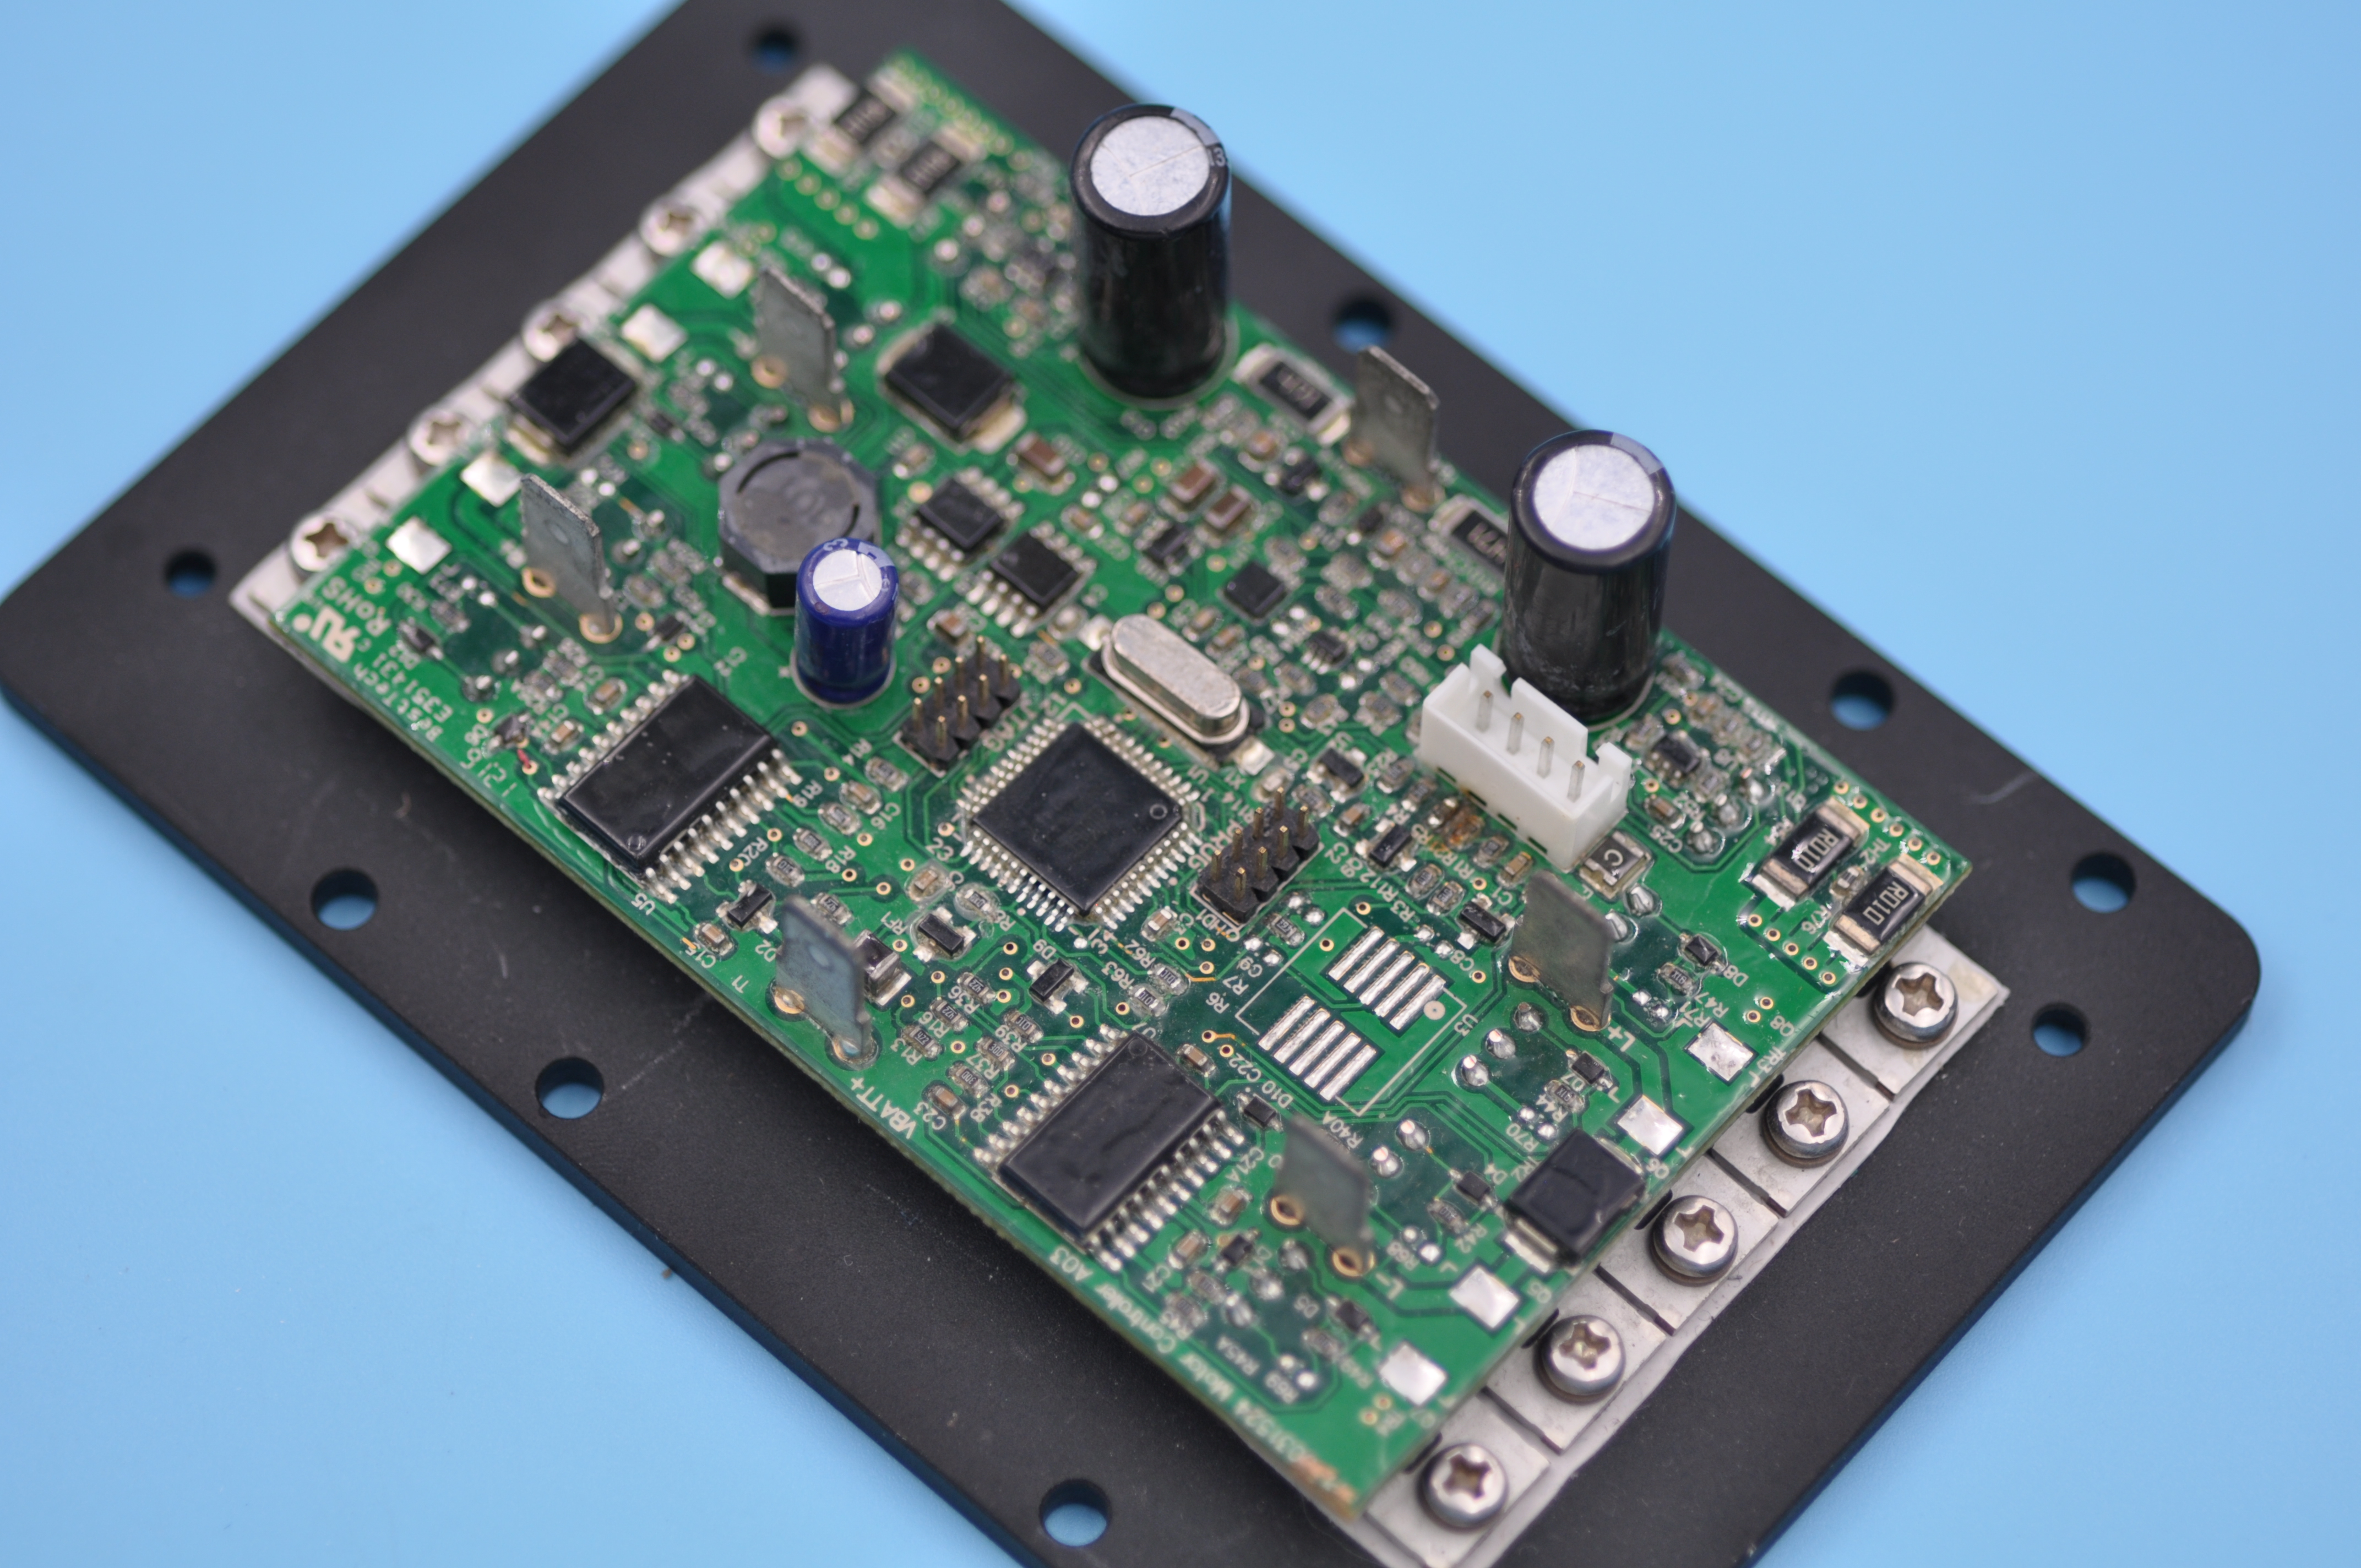
PCB Thermocouple, instrumented circuit board connected to a reflow profiling data logger

What Is a PCB Thermocouple and What Does It Measure During Reflow?

A PCB thermocouple is a welded junction of two dissimilar conductors fixed to a defined point on a populated circuit board. It records local temperature versus time at the junction; it does not measure the oven setpoint or provide one temperature for the whole assembly.

The contact point determines what the curve represents. A junction attached to a lead heel or pad can track solder-joint heating. A package-top junction checks component-body temperature. A sensor suspended above the board measures local air and cannot prove that a hidden termination reached the required soldering window.

Keep the conductors insulated up to the welded bead. If the bare wires touch before that bead, the contact can become a second measuring junction and shift the apparent location. Record the component reference, exact contact point, attachment method, channel number, and measurement purpose before the run.

Why Does PCB Thermocouple Placement Affect Temperature Measurement Accuracy?

A temperature trace is useful only when its sensing point represents the joint or component being checked. Joints connected to large copper areas may heat slowly, while exposed edge components may reach a higher peak. A well-attached sensor at a convenient but unrelated spot can still give the wrong basis for setting the oven recipe.

  • Thermal mass: Large connectors, shields, transformers, and dense component groups usually heat more slowly than small exposed devices. Place the junction on the joint or body that could limit the process.
  • Copper connection: A pad tied to a plane or heavy copper can lag behind a nearby isolated pad. Check the actual copper path instead of assuming adjacent joints behave alike.
  • Airflow exposure: Board edges, leading corners, and unshielded parts may heat faster than central or shadowed areas. Add separate points when orientation or panel position changes airflow.
  • Attachment mass: Excess solder or thick adhesive slows sensor response. The bead should touch the target directly with only enough material to hold it.
  • Measurement target: Package temperature and joint temperature are different acceptance checks. Label every channel by both location and purpose.

Where Should Thermocouples Be Placed on a PCB for Reflow Profiling?

Place thermocouples at the points most likely to narrow the reflow process window. The minimum plan covers a suspected cold joint, a suspected hot point, and any component or termination with a critical temperature requirement. Add panel positions only when copper distribution, component loading, or airflow can make them thermally different.
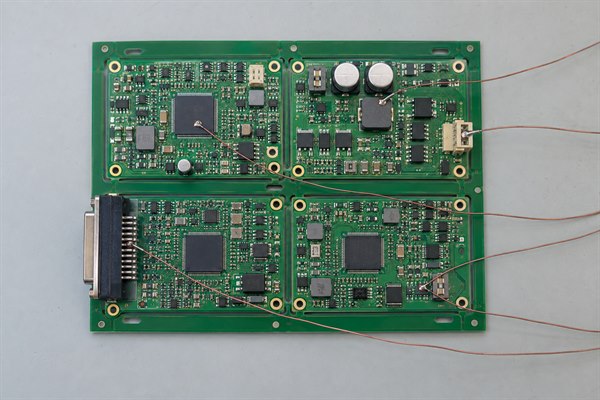
Multiple fine-wire thermocouples attached to different thermal-risk locations on a populated PCB panel

Choose candidate points from the assembly drawing, BOM, copper layout, panel orientation, and component limits. A cold-joint point matters when insufficient heat there could prevent an otherwise acceptable recipe; it need not be the lowest reading anywhere on the board.

Profile Point Recommended Location Verification Target
Cold joint Critical pad tied to a large plane, heavy copper, or high-mass component Peak and time above liquidus at the slowest relevant joint
Hot point Small exposed component or joint near a board edge Maximum temperature and available upper margin
Critical joint Exact lead heel, pad, or accessible hidden termination tied to reliability risk Solder-joint thermal exposure at the required connection
Sensitive part Specified package-body or lead location Component temperature limit
Panel variation Representative edge, center, leading, and trailing assemblies Temperature spread caused by panel position

Mark each location on an assembly drawing or photograph, including the exact contact point and why it is monitored. “TC4—U12 corner ball—cold-joint check” is more useful than “TC4” alone.

How Many Thermocouples Should Be Used for PCB Reflow Profiling?

Use enough channels to cover the thermal risks that could change the oven recipe. Roughly three to five points may cover a small, uniform assembly; a large panel or mixed-mass board may need six to twelve or more. The number depends on the actual risks, not a fixed profiling rule.

  • Cover both extremes: Include at least one predicted cold location and one predicted hot or temperature-sensitive location.
  • Add critical interfaces: Give separate channels to hidden terminations, high-reliability joints, or body limits that cannot be represented by the existing points.
  • Sample real panel differences: Add edge, center, leading, or trailing positions only where layout and airflow make a different result plausible.
  • Avoid measurement disturbance: Do not fill spare channels without a purpose. Dense wire bundles can alter airflow, pull on junctions, or interfere with the conveyor.

If the profiler lacks enough inputs, divide the plan into controlled repeat runs. Keep the oven recipe, conveyor direction, assembly state, and at least one reference channel unchanged so the groups can be compared.

Which Thermocouple Type and Wire Size Are Suitable for PCB Temperature Measurement?

Fine-wire Type K thermocouples are commonly suitable for electronics reflow profiling when they match the profiler input, connector polarity, temperature range, and insulation rating. A smaller conductor responds faster and disturbs a small joint less; a larger conductor is more durable but conducts more heat and needs more routing space.

About 0.2 mm wire is a practical choice for accessible joints; about 0.1 mm may help reach a BGA or fine-pitch target. These are examples, not required sizes. Choose a wire fine enough for the contact point but robust enough to stay attached through the planned runs.

  • Profiler match: Confirm thermocouple type, connector type, polarity, and channel configuration before installation.
  • Target access: Use finer wire when the junction must reach a hidden or closely spaced termination without bridging nearby conductors.
  • Thermal response: Keep the welded bead and exposed conductor length small enough to follow the target rather than surrounding air.
  • Mechanical life: Use insulation and strain relief that can survive the full oven cycle without softening, shorting, or contaminating the assembly.

How Should Thermocouples Be Attached and Routed on a PCB?

Fix the welded junction in direct, low-mass contact with the target and strain-relieve the wire before routing it toward the rear of conveyor travel. High-temperature solder is effective on accessible metal points; qualified high-temperature adhesive may suit package surfaces. Tape is better used for lead restraint than as the only precision contact at a solder joint.
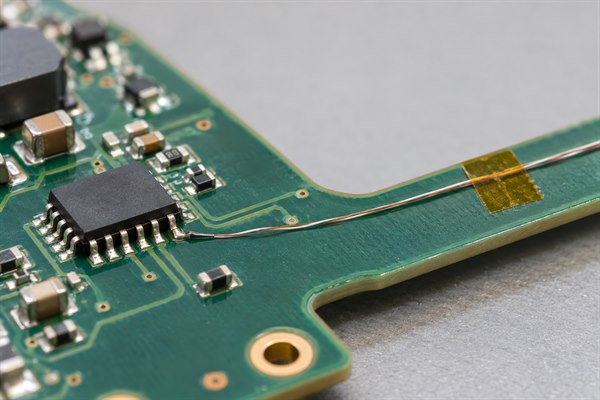
Fine-wire thermocouple junction attached to a component lead with flat routing and tape strain relief
  1. Prepare the point: Clean and identify the exact pad, lead, joint, or package location. Confirm that the selected point matches the channel plan.
  2. Attach the bead: Use the smallest secure amount of high-temperature solder or approved adhesive. Under magnification, the junction should touch the target directly.
  3. Add strain relief: Restrain the lead a short distance from the bead. A gentle pull on the cable should not move the sensing point.
  4. Route the wire: Keep it close to the board, away from moving hardware and hot oven surfaces, and clear of the local airflow being measured.
  5. Check the channel: Verify continuity, polarity, channel label, and room-temperature response before the board enters the oven.

When high-temperature solder is used, the attachment alloy must remain solid during the measured cycle. Remove incompatible low-melting solder from a sacrificial profile point where necessary, and avoid a large solder fillet that would add thermal mass.

What Thermocouple Placement Challenges Occur with BGAs, QFNs, Large Components, PCB Panels?

Hidden joints, component bodies, and panel positions cannot all be judged from the same sensing point. When a joint cannot be instrumented directly, a nearby reading can help investigate heating, but it must not be reported as that joint’s temperature.

  • BGA: A package-top sensor measures body temperature. It does not prove solder-ball temperature. Direct joint measurement may require a sacrificial assembly and controlled underside access to a selected ball.
  • QFN or LGA: An exposed perimeter pad may not represent the center thermal pad. Use underside access or a purpose-built profile sample when center-joint behavior controls the decision.
  • Large component: Connectors, transformers, and shields can create a slow joint while the component body has a separate maximum-temperature limit. Monitor both when either can restrict the recipe.
  • PCB panel: Measure representative edge, center, leading, and trailing positions when panel layout or airflow can create a meaningful thermal gradient. Compare those positions before assuming that one assembly’s profile represents every board in the panel.
  • Dense assembly: If simultaneous wiring would disturb airflow or prevent safe conveyor travel, use controlled repeat runs with a stable reference channel.

How Do You Evaluate Temperature Data from PCB Thermocouples During Reflow?

Compare each curve with the requirement for the point it actually measures. Joint traces use the selected solder-paste and alloy limits; component-body traces use the applicable component limit. Oven zone settings and conveyor speed are inputs, while the thermocouple curves show the temperature experienced by the assembly.

  • Ramp rate: Calculate the heating slope where required and check whether fast and slow locations remain within the applicable process limits.
  • Soak: Check the time and temperature range specified for the selected paste process, rather than applying a generic soak target.
  • Time above liquidus: For each critical joint, measure the interval between the trace rising above and falling below the alloy’s liquidus temperature. Compare that interval with the selected paste’s process window.
  • Peak temperature: Compare joint and package peaks with their own limits; one peak limit should not be applied to every channel.
  • Cooling rate: Review the cooling slope when it is part of the product or paste requirement.
  • Temperature spread: Compare decision-relevant channels in the same run. A cold joint and a hot package must both meet their respective limits; a small spread by itself does not prove either result.

Accept a recipe only when every critical joint and monitored package meets its own limit in the same run. If improving a cold joint pushes a component past its limit, change one controlled input—such as zone temperature, conveyor speed, or orientation—and profile again. Compare the new traces against the same channel locations and requirements.

What Causes Inaccurate PCB Thermocouple Temperature Measurements?

The most common causes are a moved junction, excessive attachment mass, damaged wiring, incorrect profiler setup, or a sensor placed on the wrong thermal object. Diagnose the trace together with the physical installation and channel record.

Trace Pattern Likely Cause Corrective Check
Abrupt step or drift Junction moved or lifted Inspect the bead and strain relief; repair and repeat
Intermittent spikes Loose connector, broken wire, or unintended conductor contact Check continuity, insulation, polarity, and connector seating
Unusually slow response Excess solder, thick adhesive, or heavy wire Compare with a lower-mass attachment at the same target
Smooth curve but poor soldering result Wrong target or surface proxy used as joint data Match the channel record and photographs to the physical contact point
Poor run-to-run agreement Attachment damage or changed loading, orientation, or board condition Repeat under controlled conditions with one stable reference channel
All channels shifted Wrong thermocouple type, logger setup, or cold-junction compensation Verify the profiler configuration and perform a known-temperature check

A smooth trace does not establish where the bead was attached. Reject a channel if its contact point cannot be confirmed after reflow, and repeat the measurement with a documented attachment.

How Can You Verify That PCB Thermocouple Measurements Are Reliable?

Check the sensor before and after reflow, confirm the profiler settings, and repeat the critical measurements. Compare runs only when the board revision, channel map, and oven recipe match.

  1. Inspect the installation: Verify bead contact, attachment size, insulation, strain relief, polarity, and connector seating. Save close-up photographs of every point.
  2. Test channel identity: At a stable room temperature, apply a controlled touch or heat stimulus to each junction. Only the expected channel should respond.
  3. Confirm the profiler: Check thermocouple type, sample interval, trigger, channel labels, and calibration status. Save the configuration with the run.
  4. Profile the real thermal load: Use the intended panel, component population, carrier, conveyor direction, and loading condition. Record any deviation.
  5. Inspect after reflow: Reject data from a junction that moved, lifted, shorted, or was damaged. Match accepted traces to the saved photographs.
  6. Repeat the run: Hold the recipe and assembly conditions constant, then compare peak, time above liquidus, ramp, and spread on the critical channels.

Reprofile when a change can alter heat transfer or the allowable window. Typical triggers include a new paste, a package or component-mass change, revised copper or stackup, a new panel layout, a different carrier, major oven maintenance, or transfer to another production line.

FAQs About PCB Thermocouple Placement and Reflow Profiling

Q1: Can a bare PCB be used for reflow profiling?

A1: A bare board cannot establish the final assembly profile. Components, solder deposits, shields, and connectors change thermal mass and airflow. Use a populated production-representative assembly or a documented equivalent profile vehicle for recipe approval.

Q2: Does changing solder paste require a new reflow profile?

A2: Reprofile if the required thermal window changes. Compare liquidus temperature, time above liquidus, soak guidance, peak range, and cooling requirements before using the existing recipe.

Q3: When does a design or BOM change require reprofiling?

A3: Reprofile when the change can affect heat transfer or a temperature limit. Large copper changes, board-thickness changes, added shields, heavier connectors, alternate packages, and revised sensitive components are common triggers.

Q4: Can a thermal camera replace attached thermocouples?

A4: A thermal camera can locate surface hot and cold regions, but it cannot automatically replace contact profiling. Emissivity, viewing angle, and line of sight limit the result, especially at hidden BGA and QFN joints.

Q5: Can the same profiling board be reused indefinitely?

A5: No. Set an inspection and retirement rule. Repeated heat cycles and handling can age the assembly, loosen attachments, and damage fine wires. Retire or rebuild the board when it no longer represents production.

Q6: What should be saved with a PCB reflow profile?

A6: Save enough data to reproduce the installation and oven run. Keep the raw traces, calculated metrics, channel map, attachment photographs, product and BOM revisions, paste identity, panel orientation, oven recipe, profiler settings, and calibration status.

For a PCBA quotation with reflow-profile or reporting requirements, send Gerber or ODB++, a BOM with exact part numbers, assembly and panel drawings, solder-paste requirements, quantity, target delivery date, and required profile or inspection records to sales@bestpcbs.com. Include any joints or component limits that need separate temperature measurements so the quotation can account for them.
You may also like

How Do You Choose an Aluminum Frame PCB Stencil?

September 15th, 2026

An aluminum frame PCB stencil holds a patterned metal foil under tension so solder paste can be printed onto PCB pads before component placement. The aluminum is the support frame, not normally the printing foil. At EBest Circuit (Best Technology), we supply custom SMT stencils and PCB assembly support. For your project, the useful starting points are printer compatibility, aperture geometry, foil thickness and the final panel layout.

Illustration of an aluminum frame PCB stencil with a mesh border and stainless steel foil

What Is an Aluminum Frame PCB Stencil?

A framed PCB stencil combines three working parts: a rigid frame, a tensioned mesh border and a thin metal foil containing openings that correspond to the solder-paste pattern. The squeegee moves paste across the foil; the openings control where paste reaches the board. After separation, the paste deposits remain on the pads.

The distinction between frame material and PCB stencil material matters when ordering. Aluminum provides a lightweight, rigid support. Stainless steel is commonly used for the PCB stencil foil because it can be fabricated with fine openings and withstand repeated printing and cleaning. A steel foil does not turn the finished circuit board into an aluminum PCB.

A PCB framed stencil is a complete mounted tool, whereas a stencil blank is an unpatterned starting material. If you need a working circuit board stencil, specify the aperture file and mounting arrangement, not just the frame dimensions.

Framed vs Frameless Stencil: Which Suits Your Production?

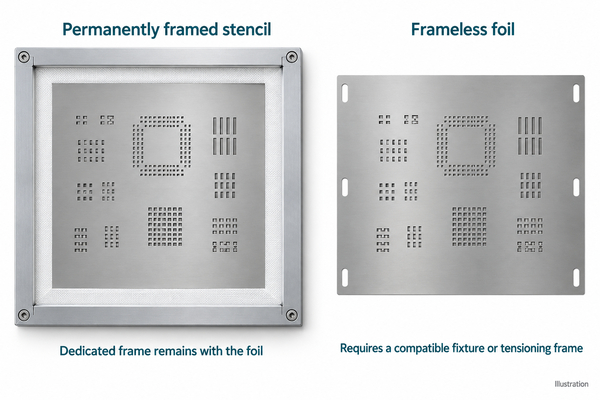
A permanently framed tool is useful for repeat builds on compatible equipment. A frameless foil can suit either a manual fixture or a reusable tensioning system, but those are different setups. Frameless does not automatically mean unsuitable for production.

Illustration comparing a permanently framed stencil with a frameless foil requiring compatible mounting
Option Best fit What to check
Permanently framed stencil Recurring assemblies with a dedicated tool Printer fit, stored-frame space, mesh and bond condition
Frameless foil in a reusable frame Multiple designs sharing compatible tensioning hardware Foil mounting interface, tensioning procedure and changeover time
Unframed foil in a manual fixture Low-volume builds and development work Flat support, registration and repeatability of the fixture

For a frameless PCB stencil printer, confirm the foil attachment system before ordering. A foil made for one tensioning system may not fit another. Prototype SMT stencils should therefore be selected around the intended printing process, not around a fixed prototype-versus-production label.

What Frame Size Fits Your Stencil Printer?

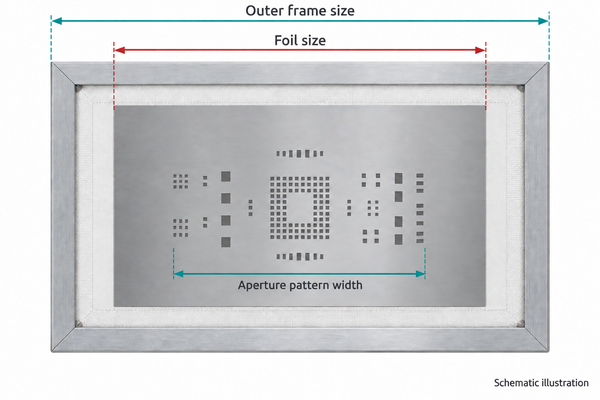
There is no single PCB stencil standard size that fits every printer. The outer frame must fit the machine clamps, while the usable printing area must accommodate the complete panel and squeegee travel. Frame profile, thickness, mounting direction and underside-cleaning clearance also affect compatibility.

Schematic distinguishing outer frame size, foil size and aperture pattern width

An SMT stencil frame drawing should distinguish the outer frame size, foil size and aperture-pattern envelope. The actual printable area is further limited by bonding margins and the printer mechanism; it is not simply the entire foil. Send the printer model or approved mounting drawing instead of ordering a frame from PCB length and width alone.

A PCB stencil holder or PCB stencil jig must support registration without bending the foil or board. For our FR4 printed circuit boards, use the released panel drawing, including rails, orientation and fiducials, when preparing the stencil. Changing the panel after cutting can make an otherwise accurate stencil unusable.

How to Choose PCB Stencil Thickness?

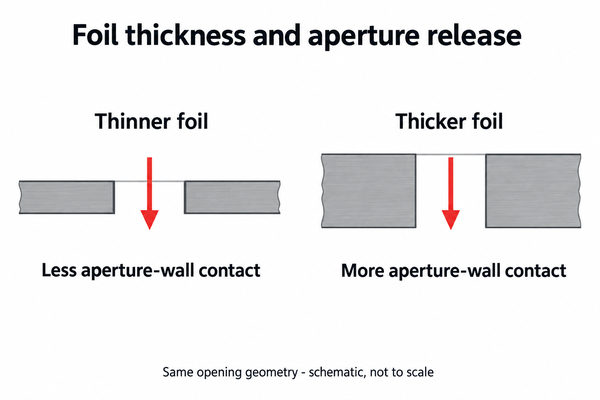
Choose thickness from the paste-volume requirements of the component mix and the release behavior of the smallest openings. A thicker foil provides more theoretical paste volume for the same aperture, but also increases the wall area that the paste must release from. More thickness is not automatically better.

Our custom SMT stencil options cover a foil-thickness range of 0.10-0.60 mm across different stencil applications, subject to engineering review. This capability range is not a recommended thickness range for every fine-pitch SMT board. We also offer step-up and step-down stencil options where different areas need different deposit volumes.

For mixed fine-pitch ICs and larger terminals, evaluate a uniform foil first, then consider local thickness changes if the requirements conflict. Step locations need clearance from nearby apertures and suitable squeegee access. Component pitch alone is not enough to select PCB stencil thickness.

How Does SMT Stencil Aperture Design Affect Paste Release?

SMT stencil aperture design determines both deposit geometry and release conditions. For a rectangular opening with length L, width W and foil thickness t, area ratio is LW / [2t(L + W)]. Aspect ratio is W/t when W is the smaller opening dimension. These describe different geometric relationships.

Schematic showing greater aperture-wall contact with thicker stencil foil for the same opening
Illustrative opening Foil thickness Area ratio Theoretical aperture volume
0.30 × 0.60 mm 0.10 mm 1.00 0.018 mm³
0.30 × 0.60 mm 0.15 mm 0.67 0.027 mm³

These calculated values illustrate geometry, not a guaranteed process window or measured deposit. Actual transfer depends on paste, aperture-wall condition, separation settings and board support. A PCB stencil thickness calculator cannot replace a print trial on the intended assembly.

For large thermal pads, multiple smaller windows may help distribute paste more appropriately than one large opening. For small pads, excessive aperture reduction can make release harder. PCB stencil design should use the component manufacturer’s land-pattern guidance, target deposit and assembly process together; a universal reduction percentage is not suitable for every footprint.

Which Fiducials and Panel Details Must Match?

PCB stencil fiducials let the printer align the foil pattern to the board. Their locations, optical contrast and marking method must suit the vision system. A fiducial is not necessarily an open hole: etching, filling or other marking arrangements depend on the printer and stencil specification.

For double-sided assemblies, identify top and bottom paste files explicitly and confirm viewing direction. Do not mirror a file merely because it is named bottom. The manufacturing output convention and assembly orientation must agree. When both sides share one foil, the printer’s working area, orientation and separation between patterns need approval.

Keep the PCB paste layer, panel drawing and assembly revision synchronized. The solder-mask layer is not a substitute for the paste layer: mask openings expose board features, while paste apertures define deposits for assembly.

How Is a Laser Cut PCB Stencil Made?

A laser cut PCB stencil is produced by cutting the approved aperture pattern into metal foil, applying the specified finishing operations and mounting the foil to its support system. In a permanently framed construction, the foil and mesh bond must maintain the required tension and flatness during use.

Our PCB stencil service includes laser-cut, etched, framed and unframed constructions, as well as electropolishing options. For a laser cut SMT stencil, electropolishing can improve aperture-wall condition, but it does not correct the wrong aperture geometry, foil thickness or panel file. The finishing requirement belongs in the order specification.

Before release, agree on the features that need verification: aperture dimensions and positions, foil thickness, image orientation, frame compatibility, bond condition and tension where specified. For fine-feature work, clarify the measurement method and acceptance criteria rather than assuming the word precision defines them.

How to Use a PCB Stencil?

The basic sequence is alignment, printing, controlled separation and deposit inspection. For a new framed tool, a short first-article print check is more useful than assuming that successful clamping proves process readiness.

  1. Confirm the stencil revision, print side and matching PCB panel.
  2. Support the board and align the apertures to the pads using the printer’s specified registration method.
  3. Apply compatible solder paste and use the established squeegee and separation settings for the assembly.
  4. Inspect deposit alignment, bridging, missing paste and consistency before placing components.
  5. Adjust the process or aperture design from the observed defect, rather than compensating for every problem with more pressure.

SMT solder paste stencils are printing tools, not reflow fixtures. The stencil is removed before placement and reflow. Through our PCB assembly services, we support SMT, through-hole and mixed assemblies; discuss stencil supply together with your assembly files when you need a coordinated PCB and PCBA order.

How Should Framed Stencils Be Cleaned and Stored?

Use a cleaning method compatible with the solder paste, foil, mesh and bonding adhesive. Residue inside an aperture can reduce the next deposit, while contamination beneath the foil can contribute to smearing. Follow the applicable cleaning-equipment and chemistry instructions, and protect personnel according to the relevant safety information.

Do not scrape fine openings with tools that can alter their geometry. After cleaning, check for blocked apertures, dents, corrosion, lifted bonding and mesh damage. A visibly clean foil is not automatically a flat, tensioned tool.

Store each tool by design, side and revision in a protected SMT stencil rack or equivalent support. Prevent contact with the active foil area. Reuse depends on condition and validated printing performance, not a universal number of print cycles. A replacement foil must also match the original mounting system.

What Affects the Price of a Framed PCB Stencil?

Price depends on frame size, foil specification, aperture complexity, finishing, step features, inspection requirements and delivery arrangements. A low tool price can be poor value if it requires a new holder, cannot fit the printer or has to be remade after a panel revision.

Compare quotations against the same drawing and scope. Ask whether the price includes the aluminum frame, patterned foil, mounting, specified finishing and inspection. For repeat orders, confirm whether an existing frame can be reused and whether that service is actually included.

For suitable stencil orders, we can provide turnaround as fast as one working day. Availability depends on the design, finishing and order review; production time is separate from transport time. Tell us the required arrival date so that the quotation can address both.

What Files Do We Need for Your Custom Stencil?

For a custom aluminum frame PCB stencil, send the released paste-layer data and final panel information first. We accept Gerber and supported PCB/CAD design files. A PDF can explain dimensions and notes, but a drawing alone may not contain the complete aperture geometry needed for manufacture.

Input Include
Design identity Part number, revision, top/bottom side and units
Aperture data Paste Gerber or supported design files, approved modifications and critical features
Panel and alignment Final panel drawing, rails, fiducials and print orientation
Printer interface Machine model, outer frame dimensions, frame profile and clamping requirements
Foil and finishing Requested thickness, step regions, surface treatment and inspection criteria
Order scope Quantity, stencil-only or PCB/PCBA supply, destination and required arrival date

If the thickness or aperture treatment is not yet defined, identify the fine-pitch devices and larger solder-volume features for review instead of guessing a specification. Send your aluminum frame PCB stencil requirements to sales@bestpcbs.com. Our team can discuss the stencil construction and manufacturing scope with you before quotation.

You may also like

How Do You Read Electrical Circuit Diagram Symbols?

September 15th, 2026

Electrical circuit diagram symbols represent components and their electrical connections, not the physical shape of a finished board. To read them, identify each symbol, follow its connected nets, then check values, polarity and pin numbers. For a PCB project, those details must remain consistent from the schematic through the component list, footprint and assembly drawing.

Electrical circuit diagram symbols on a reference sheet beside a PCB, conceptual illustration

What Are Electrical Symbols in Circuit Diagrams?

Electrical symbols are graphical shorthand for functions such as resistance, energy storage, switching and amplification. A circuit diagram uses electrical symbols to represent components and lines to show the intended connections between their terminals. A resistor drawing identifies a resistor; its label and linked part record specify which resistor belongs on the board.

Electrical symbols and electronic symbols overlap. A battery, switch or connector can appear in both a machine control schematic and a small electronic assembly. The difference is the system being described, not a completely separate alphabet. This guide concentrates on electronic circuit symbols used in PCB-related drawings rather than building floor-plan notation.

Common Circuit Symbols and Functions

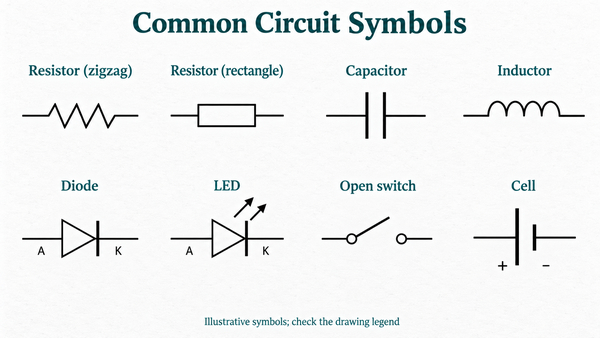
The most useful starting point is a circuit symbols chart that pairs the drawing with its function and the detail you must verify. The illustration shows basic electrical circuit diagram symbols; the table explains how to interpret them without treating the shape as a complete component specification. Together they form an electrical symbols chart with reading checks, not a list of interchangeable parts.

Original electrical symbols chart showing resistors, capacitor, inductor, diode, LED, switch and cell
Component Typical drawing cue Function and reading check
Resistor Zigzag or rectangle Limits current or establishes voltage ratios. Read resistance, tolerance and power rating.
Capacitor Two plates; polarized versions may show + Stores charge and supports filtering or coupling. Check capacitance, voltage rating and polarity.
Inductor Coil; some versions include core markings Stores magnetic energy. Check inductance, current rating and the specified part.
Diode / LED Diode with cathode bar; LED adds outward arrows Diode conduction is directional. LED arrows represent emitted light, not extra terminals.
Cell / battery Unequal parallel lines; repeated pairs for a battery Provides DC energy. The longer line indicates the positive side; voltage requires a label.
Switch Contact points and movable contact Makes, breaks or changes a connection. Identify the pole, throw and shown state.
Fuse Small inline fuse element, convention-dependent Overcurrent protection. Read current, voltage and time-current characteristics.
Transistor / IC Device-specific symbol or pin-labelled block Switches, amplifies or processes signals. Confirm pin names, numbers and supply connections.

These schematic symbols of electronic components describe electrical roles. Ratings and package dimensions belong in the component data and bill of materials (BOM); they cannot be inferred from how large the symbol is drawn.

What Is the Symbol for Electric Wire?

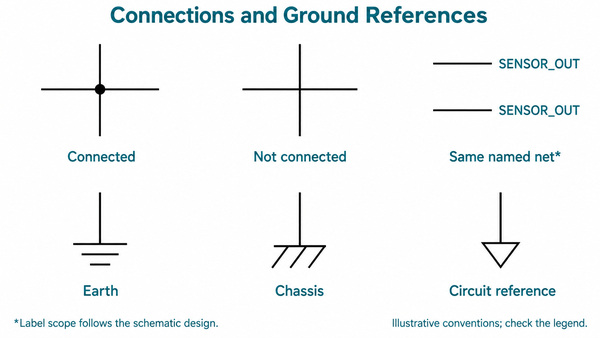
A straight line represents an electrical connection. A filled junction dot normally joins intersecting wires; crossing lines without a dot normally remain separate in modern electronic schematics. Older drawings may use a curved crossover or different junction conventions, so check the legend before tracing an unfamiliar design.

Wires that share a net label can be connected even when no continuous line runs across the page. In hierarchical designs, local, global and sheet-level labels have different scopes. Matching visible text alone does not prove that two labels on different sheets form one net.

Illustrative connected and unconnected wire crossings, matching net labels and ground reference symbols

A bus groups named signals; it is not a copper short between every signal inside it. A no-connect marker on an unused pin also differs from a junction dot. When checking an electrical schematic drawing, use net highlighting or the connection list to resolve an ambiguous intersection instead of guessing from a low-resolution image.

How Do Power, Battery and Ground Symbols Differ?

Power symbols identify sources or supply nets, while a ground symbol identifies a reference or grounding connection. Neither the position of a symbol nor the word GND alone establishes a physical connection to protective earth.

What is the symbol for battery?

The battery circuit symbol commonly uses alternating long and short parallel lines. One pair represents a cell; multiple pairs represent a battery. The number of drawn pairs is not a reliable cell-count specification, and the symbol does not establish voltage or chemistry. Read the stated supply value and battery part information.

What are symbols for AC and DC current?

A sine-wave mark commonly indicates AC, while a solid line above a dashed line indicates DC in equipment notation. Circuit source symbols may instead show a sine wave, +/− signs or a directional arrow inside a circle. The letter I is the usual current symbol in equations; it is not a component or a substitute for an AC/DC rating.

Earth, chassis and circuit-reference symbols serve different purposes. Circuit reference is the node used for voltage measurements; chassis refers to the frame or enclosure; protective earth is part of a safety connection. They may be connected by a deliberate design, but must not be assumed interchangeable. Separate AGND and DGND labels likewise require an intentional connection strategy, not an automatic split in the PCB ground plane.

How Do You Read Resistor, Capacitor and Inductor Symbols?

Read the symbol first, then the component value and its surrounding connections. Passive components with identical drawings can perform very different jobs depending on where they sit in the circuit.

Resistor symbols and adjustment arrows

The resistor schematic symbol can be a zigzag or rectangle. A diagonal adjustment arrow indicates a variable element; a potentiometer normally has two end terminals and a third wiper terminal. A fixed resistor connected from a digital input to a supply is a pull-up, while the same component in series with an LED limits current.

For readers asking what schematic symbol represents a current limiter, there is no single answer for every circuit. A series resistor can limit current, but regulated current limiting may use an IC, transistor and sense resistor. The circuit function must be established from the connections and ratings.

Capacitor and magnetic-component details

A non-polarized capacitor symbol uses two plates. Polarized versions may add a + sign and sometimes a curved plate; the explicit polarity marking and component datasheet take priority. A ceramic capacitor is not made polarized simply by the orientation of its label.

An inductor symbol is commonly a coil. Added core markings distinguish some symbol variants; two coupled windings indicate a transformer. Dots on coupled windings describe relative winding polarity, not junctions connecting the windings. A symbol alone does not specify saturation current, insulation rating or the complete magnetic construction.

How Do Diode and LED Symbols Show Polarity?

The diode’s bar identifies the cathode, commonly labelled K; the other terminal is the anode, A. Conventional forward current passes from anode to cathode when the device is appropriately forward biased. Rotating the symbol changes its position on the page, not the terminal identities.

The LED symbol adds arrows pointing away from the diode to indicate emitted light. A photodiode uses arrows pointing toward it. Zener and Schottky devices use modified cathode markings, so a generic diode sketch is not enough to identify the correct BOM part.

Before PCB assembly, match the schematic polarity to the footprint pad numbering and the component drawing. Do not assume every library assigns pin 1 to the same terminal. Our rectifier diode guide covers the additional voltage, current and recovery checks needed for rectification circuits.

How Do Switch, Relay and Protection Symbols Work?

A switch symbol shows which contacts connect in the illustrated state. SPST has one switched path; SPDT connects one common terminal to either of two alternatives. Pole and throw describe the contact arrangement, not the number of decorative lines or package pins.

What is the symbol for a single pole switch?

For a simple SPST switch, two contact points and a movable line show an open or closed path. Normally open and normally closed refer to a defined normal condition, commonly an unactuated switch or de-energized relay. Read any drawing note that specifies a different state.

In electrical control circuit diagram symbols, a relay coil and its contacts may be drawn far apart and linked by a common reference. Their physical separation on the schematic does not mean they are separate devices. A limit switch adds an actuation function; the associated mechanical state still needs to be understood.

A fuse and a circuit breaker symbol both concern protection, but they do not describe interchangeable parts. A fuse is normally replaced after operation; a breaker may be reset after the fault is addressed. Contact symbols do not establish safe working voltage, interrupting capacity or regulatory approval.

How Are Transistors, Logic Gates and IC Pins Represented?

Active-device symbols identify functions and terminal relationships. The pin names and part-specific pinout are what connect the drawing to the real package.

On a bipolar transistor, B, C and E identify base, collector and emitter. The emitter arrow points outward for NPN and inward for PNP. A MOSFET uses gate, drain and source, and its symbol may show a body diode. Its appearance is not permission to swap source and drain.

Logic circuit symbols distinguish AND, OR, inversion and other functions. A small output bubble indicates inversion; a triangle without that bubble may be a buffer. An operational amplifier also has a triangular body, but its + and − inputs and supply requirements identify a different function. Those input signs are not the amplifier’s power pins.

Large ICs are often rectangular blocks with named and numbered pins. One physical package may be split into several schematic units, including a separate power unit. For fine-pitch devices on HDI PCBs, accurate pin-to-pad mapping must precede escape routing: the logical symbol does not determine the required via structure.

Why Do IEC and ANSI-Style Schematic Symbols Look Different?

Different symbol conventions can represent the same electrical function. The familiar resistor rectangle is associated with IEC-style drawings, while the zigzag is common in ANSI/IEEE-style drawings. Neither shape alone changes resistance or selects a regional component.

IEC 60617 concerns graphical symbols for electrotechnical diagrams. CAD libraries and legacy documents may use different variants, particularly for logic, grounding and switches. Follow the drawing’s stated convention and legend rather than expecting every electrical schematic symbols chart to look identical.

For an unfamiliar symbol, first check its reference, terminal names and linked part number, then compare it with the library definition. A copied image can omit a polarity mark, inversion bubble or connection dot that changes the interpretation.

What Do R1, C1, Values and Pin Numbers Mean?

A reference designator identifies one component instance; a value describes an electrical property; a pin number maps a terminal to the package. Mixing these three kinds of circuit notation is a common cause of schematic-to-BOM errors.

Marking Meaning What to confirm
R1, C1, L1, D1 Common references for resistor, capacitor, inductor and diode The same reference identifies the same part in the BOM and PCB files.
U1, Q1, J1 Common references for an IC, transistor and connector Project conventions vary; check the library and assembly drawing.
4k7 / 4R7 4.7 kΩ / 4.7 Ω Do not confuse a multiplier with a reference prefix.
100 nF / 0.1 µF The same capacitance value Voltage, dielectric and tolerance still need specification.
Pin 1 / A / K Package number or functional terminal name Check the selected symbol-to-footprint mapping; do not infer numbering from left/right position.
DNP / DNI Do not populate / do not install Ensure assembly variants agree across BOM, drawing and placement data.

A value is not a complete purchasing description. Two 10 kΩ resistors can differ in package, tolerance and power rating. For multi-unit devices, make sure the separate units still resolve to one physical part and that all supply pins are accounted for.

How to Read Circuit Diagrams?

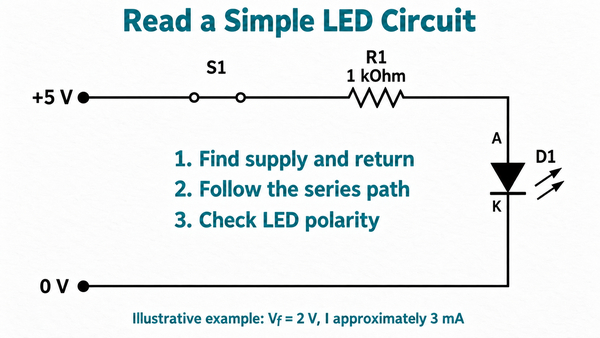
Trace a complete path from the supply through the load and back to the return, checking the state of each component along the way. This gives the individual symbols a circuit-level meaning.

Illustrative closed-switch LED circuit with 5 V supply, 1 kilohm resistor and approximately 3 mA under stated assumptions
  1. Find the +5 V supply and 0 V return. The source is connected at the two labelled terminals.
  2. Follow S1. It is shown closed, so the series path continues through R1.
  3. Read R1 as 1 kΩ. It limits the current rather than setting the LED voltage directly.
  4. Identify D1’s anode and cathode. The cathode bar is on the return side.
  5. Estimate current using the stated assumptions: I = (5 V − 2 V) / 1,000 Ω = 3 mA.
  6. Check what changes when S1 opens: the series path is broken and the ideal steady-state LED current becomes zero.

The 2 V LED forward drop is an illustrative assumption, not a value for every LED. Actual current depends on the selected LED, supply tolerance, resistor tolerance and temperature. The resistor dissipates approximately 9 mW in this example; its selected rating still needs suitable operating margin.

To draw a circuit diagram, place symbols from the appropriate library, connect their electrical pins, add values and annotate references. Run electrical rules checking (ERC), then inspect the circuit function. ERC can find certain connection conflicts but cannot prove that the design will perform as intended.

How Do Schematic Symbols Become a Manufacturable PCB?

A schematic defines logical connectivity; a PCB layout defines physical pads, tracks, vias and placement. A wiring diagram instead emphasizes connections between terminals, cables or assemblies. Wiring diagram symbols can overlap with schematic notation, but the documents answer different questions.

For FR4 printed circuit boards, the net information must be translated into copper geometry with suitable spacing, current capacity and return paths. A neat electrical schematic diagram does not, by itself, establish board thickness, layer stack-up or trace dimensions.

At EBest Circuit (Best Technology), we provide PCB assembly services for SMT, through-hole and mixed assemblies. Our assembly capability includes 01005 SMD components and BGA pitch down to 0.25 mm, subject to review of the actual package, PCB and process requirements. Clear polarity, pin mapping and assembly-variant information are particularly important for small components and dense packages.

For a fabrication and assembly quotation, send your current Gerber and drill files, BOM with manufacturer part numbers, pick-and-place data and assembly drawing. Include the schematic and any special test or polarity requirements so we can discuss ambiguities against the same design revision. A schematic screenshot alone is not a complete manufacturing package.

Reading electrical circuit diagram symbols is the first step; consistent component and manufacturing data keep that meaning intact on the finished board. Send your project files to sales@bestpcbs.com for PCB and assembly review.

You may also like

What Is a Rectifier Diode and How Does It Work?

September 15th, 2026

A rectifier diode is a semiconductor component that conducts mainly in one direction and blocks reverse current within its voltage rating. It is used to turn AC into a unidirectional, pulsating output. On a PCB, its performance depends on more than the part number: current, switching speed, polarity, copper paths and cooling must work together.

Rectifier diode concept illustration showing axial and surface-mount packages on a PCB

What Is a Rectifier Diode?

A rectifier diode is a diode selected for power rectification rather than primarily for processing small signals. Its two terminals are the anode and cathode. An individual diode is a component; a diode rectifier can be a complete circuit containing several devices, or an integrated bridge package.

In a PCB power supply, rectification is only one stage. Filtering reduces ripple, and a regulator controls the output voltage. A diode alone does not provide a smooth, regulated supply or electrical isolation.

How Does a Rectifier Diode Work?

The rectifier diode function follows its bias condition. With sufficient forward bias, conventional current flows from anode to cathode. Reverse bias greatly reduces that current, but leakage remains; exceeding the device’s reverse-voltage capability can damage it.

What does a rectifier diode do when the input alternates? In a simple series circuit, it passes one half-cycle and blocks the other. Arranging multiple devices into a full-wave circuit lets both input half-cycles deliver current through the load in the same direction.

Forward voltage is not a fixed 0.7 V. It changes with current, temperature and diode technology. A PN device also takes time to remove stored charge when switching from conduction to blocking, so a diode that suits a low-frequency supply may be unsuitable in a switching converter.

What Does the Rectifier Diode Symbol Mean?

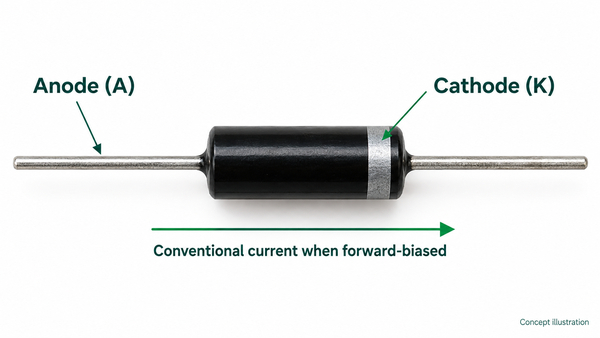
The rectifier diode symbol identifies the anode and cathode; the straight bar marks the cathode. On many axial rectifiers, a band on the body identifies that same terminal. Match the symbol, package drawing and PCB footprint before assigning placement orientation. The rectifier diode diagram below relates the physical band to the two terminals.

Rectifier diode diagram relating the axial cathode band to anode and cathode terminals

A rectifier diode number such as 1N4007 identifies an electrical device family, not a complete footprint specification. Supplier suffixes can change packaging and lead details. For SMD parts, confirm the manufacturer marking drawing rather than relying on a stripe convention alone. A readable polarity mark on the assembly drawing helps prevent a correct component being fitted backward.

How Do Half-Wave and Full-Wave Rectifier Circuits Differ?

A half-wave circuit uses one input half-cycle; a full-wave circuit uses both. In a single-phase rectifier diode circuit, the common full-wave choices are a four-diode bridge or a two-diode circuit with a center-tapped transformer secondary.

CircuitDiodes and sourceEffect on the load
Half-waveOne diode with an AC sourceOne pulse per input cycle; larger gaps between charging pulses
Full-wave bridgeFour diodes; no center tap requiredTwo pulses per cycle; two diodes conduct in series in each current path
Center-tapped full-waveTwo diodes and a center-tapped secondaryTwo pulses per cycle; each half-secondary conducts on alternate half-cycles
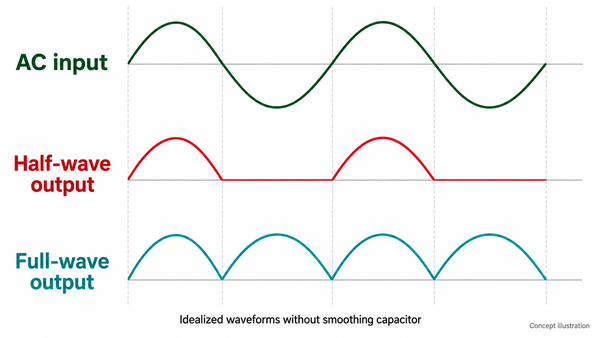
Conceptual comparison of AC input, half-wave output and full-wave output without a smoothing capacitor

How Many Diodes Are Used in a Bridge Rectifier?

A single-phase diode bridge rectifier uses four diodes. Its two alternating current paths each contain two conducting devices. This full wave bridge rectifier arrangement is convenient, but its two forward drops can be significant on a low-voltage rail.

In half wave rectifier diode selection, account for the interval in which the load receives no input energy. In full wave rectifier diode selection, consider which winding and diode pair carry current at each instant. A bridge rectifier diode must handle the charging pulses as well as the reverse-blocking interval.

A smoothing capacitor changes the current waveform: the diodes recharge it in pulses near the AC peaks. Diode peak current can therefore be much higher than the average load current. Ripple and inrush must be considered together, not solved by choosing a larger capacitor alone.

Which Rectifier Diode Types Suit Your Circuit?

Rectifier diode types differ in switching behavior and losses. Start with the circuit frequency and reverse voltage, then compare forward loss, leakage and package cooling.

TechnologyTypical fitMain selection trade-off
Standard silicon PN rectifierLow-frequency AC rectificationLow cost, but recovery may be too slow for a switching stage
Fast or ultrafast PN rectifierSwitching power conversionRecovery charge and softness must be weighed against forward loss
Silicon Schottky rectifierLow-voltage rails and fast switchingLow forward loss can be useful; reverse leakage rises with temperature
SiC Schottky rectifierHigher-voltage, high-frequency conversionAssess switching loss, conduction loss, cost and thermal design together

Rectifier Diode vs Diode: What Is the Difference?

A rectifier is one use of a diode, not a separate opposite category. A small-signal switching diode is optimized for a different combination of current, capacitance and speed. A silicon rectifier diode cannot be replaced safely just because another diode has the same outline.

Rectifier Diode vs Schottky Diode

A Schottky rectifier diode is itself a rectifier. Compared with a conventional PN part, a silicon Schottky device often offers lower forward voltage and avoids minority-carrier storage recovery, but capacitive switching current still exists. Verify leakage at the expected temperature rather than assuming the lowest forward drop always produces the coolest design.

How Do You Distinguish Between Zener Diode and Rectifier Diode Functions?

A Zener diode is designed to operate in controlled reverse breakdown for voltage-reference or clamping tasks. A conventional rectifier normally works in forward conduction and reverse blocking. Swapping these roles without checking ratings can destroy the device or stop the circuit working.

Is 1N4007 a Rectifier Diode?

Yes. The 1N4007 rectifier diode is a common general-purpose silicon PN rectifier. A representative DO-41 version has a 1,000 V repetitive peak reverse-voltage rating and a 1 A average forward-current rating, with the current rating tied to specified mounting and temperature conditions.

For this DO-41 example, the 1 A condition uses 9.5 mm leads at 75°C ambient; maximum forward voltage is 1.1 V at 1 A under the stated electrical test conditions. These are device limits, not a promise that any small PCB can deliver a continuous 1 A DC output. Check the exact manufacturer’s datasheet, derating curve and rectifier circuit before substitution.

Its familiar part number does not make it the default for high-frequency rectification. Standard recovery, package dissipation and surge loading may matter more than its high reverse-voltage rating.

How Do You Select Rectifier Diode Ratings?

Select the device against the actual circuit waveform and temperature, not just the nominal supply voltage. The key ratings answer different questions.

ParameterWhat to check
VRRMWorst repetitive reverse voltage, including circuit topology and expected transients; do not compare only with AC RMS voltage
IF(AV)Average forward current under the specified cooling, waveform and temperature conditions
IFSMNon-repetitive surge capability for the stated waveform and duration; not a continuous operating rating
VFForward loss at operating current and junction temperature
IRReverse leakage at operating voltage and temperature
trr and QrrReverse recovery time and charge under comparable test conditions
Tj and thermal resistanceAllowable junction temperature and the actual path from device to board, enclosure or heatsink

For a simple conduction-loss estimate, average the instantaneous product of diode voltage and current over time. Using VF × average current can be a first approximation when VF is represented appropriately; it does not include recovery or reverse-leakage losses. High-frequency designs need those additional terms.

Rectifier diode price also depends on package, qualification, voltage class and order quantity. A lower component cost is not a saving if it requires more cooling, a larger board or a different assembly process.

How Should Rectifier Diodes Be Laid Out on a PCB?

Give the rectifier a short current path, adequate copper and an unambiguous footprint. The board must carry pulsed current and remove heat without compromising insulation spacing.

For many control and low-power supply designs, FR4 printed circuit boards provide the required routing and mechanical support. Size conductors for the actual current waveform, copper thickness, allowable temperature rise and surrounding layout. Minimum fabrication line width is not a power-trace recommendation.

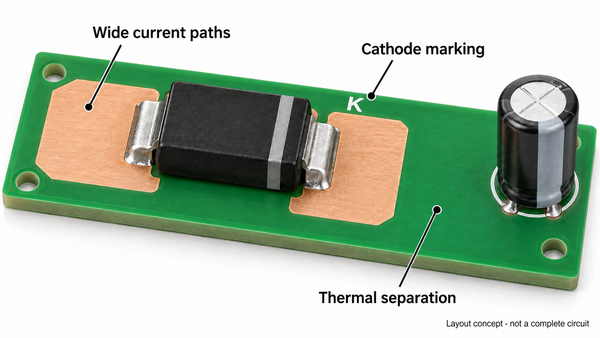
Conceptual PCB rectifier layout highlighting wide copper paths, polarity markings and separation from heat-sensitive capacitors
  • Keep the bridge-to-reservoir-capacitor charging loop compact, including its return path.
  • Use the specified land pattern and thermal-pad connection; do not add copper that bridges different electrical nodes.
  • Separate hot rectifiers from electrolytic capacitors and temperature-sensitive circuitry where practical.
  • Determine clearance and creepage from working voltage, environment and the applicable product requirements; do not use one spacing for every supply.
  • Make the cathode orientation consistent across schematic, silkscreen, assembly drawing and placement data.

For higher-current paths, our heavy copper PCBs provide 4–10 oz copper options, subject to review of the complete design. Thicker copper can help current distribution and heat spreading, but it does not remove the diode’s junction-temperature limit. Wider conductors, pad geometry and soldering heat demand must be considered together.

How Do You Test a Rectifier Diode?

A multimeter’s diode mode can reveal a gross short or open circuit, but it does not prove the device will meet its high-voltage, current or switching ratings. Disconnect power, safely discharge stored energy and verify that no voltage remains before testing. Mains-connected supplies require qualified handling.

  1. With the isolated diode in forward bias, connect the red probe to the anode and the black probe to the cathode.
  2. Read the forward-voltage indication and compare it with the expected device technology and the meter’s test conditions.
  3. Reverse the probes. A normal reverse-blocking result usually appears as an over-range indication.
  4. If the result is ambiguous in circuit, isolate a terminal using an appropriate rework procedure; parallel paths can mislead the reading.

A near-zero reading both ways can indicate a short. Over-range both ways can indicate an open diode, but poor contact or insufficient meter test voltage can produce a similar result. Board-level diagnosis should also check solder joints, polarity and the surrounding circuit. A successful diode-mode reading does not replace a powered functional test under controlled conditions.

What Happens When a Diode Shorts in a Bridge Rectifier?

A shorted diode can create a heavy fault-current path during part of the AC cycle, potentially operating a fuse or damaging other components. Disconnect the supply and investigate the bridge and surrounding circuit before replacing parts; do not keep energizing the board to see whether the fault clears.

How Do We Build PCBs for Rectifier Circuits?

At EBest Circuit (Best Technology), we manufacture the PCB and assemble the specified components into your power-conversion circuit. Our PCB assembly services cover SMT, through-hole and mixed assembly, so an axial rectifier, an SMD diode and larger connectors can be incorporated into one board build.

We check incoming components against your BOM and support inspection and functional testing as part of the agreed assembly scope. Provide the exact diode part number, board files, polarity information and operating requirements so we can review the build consistently. Component selection remains tied to the approved design; we do not substitute a familiar diode number solely because the footprint fits.

For your next rectifier diode PCB project, send the fabrication files, BOM and assembly drawings to sales@bestpcbs.com. We can help connect the required copper construction, component mounting and assembly requirements in one manufacturing review.

You may also like

How Does IPC-SM-840C Apply to PCB Solder Mask?

September 11th, 2026

IPC-SM-840C is the C revision of the specification for qualifying permanent solder mask used on printed circuit boards. It connects the coating’s electrical, physical and environmental performance with its intended application. For your PCB, the practical questions are which mask class applies, how the coating fits the layout, and whether it is compatible with fabrication and assembly. At EBest Circuit (Best Technology), we provide PCB manufacturing and assembly support to help turn those requirements into a buildable board.

Conceptual illustration of IPC-SM-840C solder mask on a printed circuit board

What Is IPC-SM-840C?

IPC-SM-840C addresses the qualification and performance of permanent polymer solder mask, also called solder resist. The coating covers selected copper and laminate surfaces while leaving soldering pads, contacts and other specified areas exposed. It helps protect conductors and define where solder should wet during assembly.

The C revision dates to January 1996, with Amendment 1 issued in June 2000. It is a historical edition, so an existing drawing may name it even when a current material datasheet names a later revision. The standard concerns both material evaluation and the way the mask is used on a board. For example, a coating qualified on a test substrate still needs a suitable application process on the actual copper pattern.

What Do IPC SM 840 Classes T and H Mean?

Class T and Class H distinguish solder mask performance requirements by end-use reliability needs. Class T covers telecommunications and other high-performance commercial or industrial equipment. Class H addresses high-reliability applications where continued operation is critical. For drawings that specify IPC-SM-840C Class T or IPC SM 840C Class H, the required designation should carry through to the selected mask material.

Solder mask classApplication emphasisWhat to specify for your board
IPC SM 840 Class TLong service life in commercial and industrial electronicsRequired revision, compatible mask material and intended assembly conditions
IPC SM 840 Class HHigher assurance where uninterrupted operation is essentialRequired revision and class, with the qualification evidence applicable to that material and process

These letters describe the solder mask requirement. The finished PCB’s IPC-6012 Class 2 or Class 3 requirement is a separate specification covering the rigid board. Keeping both requirements explicit makes the intended coating performance and overall board quality clear.

Which Solder Mask Properties Affect PCB Reliability?

Adhesion, electrical insulation and resistance to processing exposure determine whether the coating can protect the circuit throughout manufacture and use. Colour and surface appearance matter for inspection and product presentation, but the functional properties are the basis for material selection.

Property groupWhat it addressesRelevance to the finished PCB
Adhesion and mechanical integrityBonding to the underlying surface; resistance to cracking or peelingMaintaining coverage around tracks, pads and machined edges
Electrical performanceDielectric strength and insulation resistanceHelping preserve insulation between neighbouring conductors
Soldering and chemical resistanceExposure to soldering heat, fluxes and process chemicalsKeeping the mask intact through board finishing and assembly
Environmental performanceMoisture exposure, thermal changes and electrochemical migrationMatching the material to the board’s service conditions
Cure and surface conditionDeveloped film properties and usable surface qualitySupporting consistent handling and subsequent processing

For our FR4 printed circuit boards, solder mask selection belongs alongside copper layout, surface finish and assembly requirements. A controller with exposed test points has different mask artwork needs from a densely populated communications board, even when both use the same laminate family.

How Does LPI Solder Mask Become a Protective Pattern?

Liquid photoimageable solder mask is applied as a coating and patterned by light exposure and development. A typical LPI soldermask process includes surface preparation, coating, preliminary drying, imaging, development and final cure. The result is a permanent film with openings matched to the circuit artwork.

Surface preparation supports adhesion; imaging and development define the openings; final cure develops the required film properties. Their combined effect explains why the material name alone is only part of the finished-board result. Dry-film photoimageable solder mask offers another material format, with different behaviour over the board’s raised copper features.

The phrase LDI vs LPI solder mask can cause confusion: LPI describes liquid photoimageable material, while laser direct imaging describes an imaging method. An appropriately formulated LPI material can be used with direct imaging. Material selection and imaging compatibility therefore need to be considered together.

What Is the Recommended Thickness for PCB Solder Masks?

The recommended finished thickness is material- and layout-specific; one universal value does not describe every PCB. Solder mask thickness affects protection over copper edges, available clearance and the local surface height around component pads. A patterned PCB is not flat: copper traces, planes and gaps create different coating conditions. Thickness over a conductor and thickness beside it may therefore differ.

Not-to-scale conceptual cross-section showing solder mask covering raised copper traces and laminate

An IPC SM 840 solder mask thickness requirement should identify the measurement location and the agreed finished-film requirement. A value measured over bare laminate is not directly interchangeable with one measured over copper. The material system, copper profile and circuit geometry determine the practical coating window.

This becomes especially relevant on our heavy copper PCBs: taller conductors make edge coverage and coating transitions more demanding. Providing the outer-layer copper requirement with the mask artwork allows these features to be considered together, rather than treating the mask as a uniform flat sheet.

Why Do Pad Openings and Mask Dams Matter?

Pad openings expose the intended solderable surface, while a solder mask dam is the narrow strip of coating between adjacent openings. Registration is the alignment between the mask pattern and the copper pattern. Together, these features influence usable pad area and separation around fine-pitch components.

Conceptual top view of fine-pitch solder pads with separate openings and green solder mask dams

For our HDI boards, the pad pitch, opening size and achievable registration must work together. If a proposed dam is too narrow to manufacture consistently, the layout or opening strategy needs adjustment. The package’s land-pattern requirements remain important, particularly when choosing solder-mask-defined or non-solder-mask-defined pads.

Via tenting is a separate artwork choice: mask covers the via opening rather than filling the hole. Keep probe-access test points exposed, and specify via filling separately where that structure is required. These details help us preserve both assembly access and the intended coverage during DFM review.

How Do Surface Finish and Assembly Affect Mask Selection?

The mask must tolerate the selected board-finishing process and subsequent assembly exposure. ENIG, immersion tin and HASL use different chemical or thermal processing routes. Reflow, wave soldering and cleaning add further conditions after the bare board has been manufactured.

We offer finishes including ENIG, lead-free HASL, OSP, immersion silver and immersion tin. Sharing your intended finish and assembly route helps us discuss the appropriate board construction and mask compatibility. For a mixed SMT and through-hole assembly, the total processing sequence matters more than considering one reflow pass in isolation.

Mask colour can also affect imaging and cure settings within a material family. A green-to-black or green-to-white change is therefore a material/process choice as well as a cosmetic one. Its effect on fine features should be reviewed with the board requirements.

Solder Mask vs Conformal Coating: What Is the Difference?

Solder mask protects selected areas of the bare PCB and defines soldering openings. Conformal coating is normally applied after assembly to protect the populated board from its environment. They occupy different places in the build and can be used together.

Conceptual comparison of solder mask on a bare PCB and a translucent protective coating over an assembled circuit

For an industrial sensor exposed to humidity, the bare board may use solder mask while the completed assembly receives a compatible conformal coating. Connectors and test interfaces can require selective exclusion from that later coating. Adhesion between the two coatings and compatibility with cleaning residues become part of the assembly design.

Our PCB and PCBA services let you discuss bare-board manufacture and assembly as a connected project. Where additional protective coating is required, include that requirement with the assembly information so the intended materials and exposed areas are clear.

IPC SM 840 Latest Version: Is Revision C Still Current?

No. As of September 2026, the IPC document revision table lists revision E, issued in December 2010, after revision D from April 2007. C remains relevant to legacy specifications, but new project documentation should identify the edition actually required.

In the IPC SM 840 family, IPC SM 840C was followed by IPC SM 840D and IPC SM 840E. Revision E’s scope includes flexible cover materials as well as permanent solder mask. The revision letter therefore conveys technical scope, not merely a newer publication date.

If your drawing calls for C and the proposed mask documentation references E, send both with the project files. We can discuss the specified material and manufacturing route with you; any change to the drawing’s requirement should be agreed before production. The selected edition and class provide a clearer requirement than simply writing “IPC solder mask.”

How Can We Support Your PCB Solder Mask Requirements?

We combine PCB manufacturing, DFM support and assembly services, helping you match the solder mask pattern to the actual circuit. Our FR4 capability extends to 32 layers, and our HDI capability includes minimum line/space down to 2/2 mil, subject to materials, stack-up, board dimensions and engineering review. These are circuit-fabrication capabilities; the mask opening and dam requirements are reviewed separately.

For a board specified to IPC-SM-840C, send the Gerber files, fabrication drawing, required class, mask colour, surface finish and any critical pad or via details. Add assembly files when PCB assembly is part of the project. Contact our team at sales@bestpcbs.com or through our PCB manufacturing enquiry page to discuss your board.

You may also like

What Does IPC-6012 Class II Mean for Your PCB?

September 11th, 2026

IPC-6012 class II identifies a performance level for rigid printed circuit boards used in dedicated-service electronics. Usually written Class 2, it addresses the quality of the manufactured bare board, including its conductors, plated holes, insulation and structural integrity. It is not simply an appearance grade. At EBest Circuit (Best Technology), we manufacture PCBs and help you connect the specified performance class with a practical board construction, so your assembly starts with the right foundation.

Conceptual illustration of IPC-6012 Class II rigid PCB quality with a plated board and inspection coupon

What Is IPC-6012 Class II?

IPC-6012 Class II means the Class 2 requirements within the qualification and performance specification for rigid printed boards. Class 2 serves equipment where dependable operation and an extended service life matter, but uninterrupted operation is not as critical as it is for Class 3 applications. The numeral II does not mean a two-layer board or revision two of the standard.

IPC 6012 class 2 can apply to different rigid constructions, from a double-sided controller board to a multilayer interconnect. Layer count, laminate grade and surface finish still need their own specification. A Class 2 designation therefore answers one important question about acceptance, but does not define every feature of your PCB.

Which Products Are Suitable for Class 2 PCBs?

Class 2 is a relevant starting point for many commercial instruments, communications peripherals and industrial controls whose service requirements match dedicated-service electronics. The application name alone does not determine the class: the consequence of failure and the required operating conditions matter more.

Application exampleWhat the PCB contributesWhat still needs application-specific attention
Commercial measurement instrumentStable connections between sensing, conversion and display circuitsLeakage paths, noise-sensitive layout and calibration requirements
Communications peripheralInterconnects for processing, power and external interfacesControlled impedance, connector loading and signal integrity
Non-safety-critical industrial controllerReliable mounting and connections for control and input/output circuitsTemperature cycling, contamination and terminal mechanical loads
Conceptual industrial controller assembly showing a rigid PCB application, not a customer product or conformity claim

For these types of circuits, our FR4 printed circuit boards provide a manufacturing route from prototypes to multilayer builds. We review the board design against the requested construction; an instrument’s safety function or environmental exposure may require additional requirements beyond a general Class 2 designation.

What Do IPC 6012 Class 2 Requirements Cover?

IPC 6012 class 2 requirements cover the finished bare board’s physical and electrical quality, not just its visible surface. The areas below explain why a board can look acceptable yet still need evidence about its internal connections or insulation.

Quality areaExamples of relevant featuresValue to your product
Conductors and spacingTrace geometry, copper continuity and separationMaintains intended current paths and reduces short-circuit risk
Holes and interconnectionsHole copper, registration and connection to internal landsSupports reliable connections between layers and component leads
Laminate and structureBonding integrity and response to specified thermal stressReduces vulnerability to internal damage during subsequent processing
Solderable surfaces and maskSurface condition, coverage and mask alignmentProvides a suitable foundation for component assembly
Dimensions and flatnessFinished geometry, hole position, bow and twistHelps the board fit fixtures, connectors and the enclosure
Electrical performanceContinuity and insulation-related requirementsChecks conditions that appearance cannot establish

The applicable revision and your agreed drawing determine the actual acceptance limits. Our PCB testing capabilities include AOI, microsection analysis and flying-probe testing. These address different types of evidence; a continuity pass alone does not demonstrate every structural requirement.

Why Are Hole Copper and Annular Rings Important?

A plated hole is an electrical connection through the board, while its annular ring is the copper land around the hole. Their geometry and integrity affect whether a connection remains reliable after soldering and use. Drilling, layer registration and plating all contribute to the finished result.

Conceptual four-layer PCB cutaway with a continuous plated through-hole and annular ring; not to scale

The copper weight chosen for a surface layer is not the same measurement as hole-wall plating thickness. Likewise, a round pad in the design file does not guarantee the same annular ring after drill and registration tolerances. Preserving manufacturing allowance around these features helps avoid late layout changes and marginal interconnections.

For our HDI boards, the connection between a microvia and its target land is also important. A small surface footprint can save routing space, but microvia construction needs its own engineering review; it should not be treated as a scaled-down conventional through-hole with identical behavior.

How Do Laminate and Thermal Stress Affect Reliability?

The laminate must maintain insulation and structural integrity through the thermal conditions relevant to the build. Copper and resin expand differently, so soldering heat places stress on the board and its interconnections. This is why material selection and plated-hole quality work together rather than as separate purchasing choices.

Conceptual rigid PCB in a thermal chamber illustrating thermal exposure; not an actual factory test or a specified IPC test setup

Our high-Tg PCBs are relevant when the assembly and operating conditions call for a suitable higher-Tg laminate. However, Tg alone is not a complete reliability rating: moisture behavior, thermal expansion, board thickness and the soldering profile also matter. A higher-Tg material does not automatically turn a Class 2 board into Class 3.

For your product, the useful distinction is between the specified board qualification evidence and the environment the assembled equipment will actually encounter. Repeated field temperature cycles or a harsh environment may need additional validation even when the bare board meets its agreed acceptance requirements.

IPC 6012 Class 2 vs Class 3: Which Fits Your Application?

The central difference in IPC 6012 class 2 vs class 3 is the required level of service performance and the associated acceptance criteria. Class 3 is intended for applications where continued operation is more critical. It is not simply the same board with a better finish or an extra final inspection.

DecisionClass 2Class 3
Service expectationDependable operation and extended serviceHigher-performance service where continued operation is critical
Design and fabrication impactFeatures must meet the agreed Class 2 requirementsSome features need tighter acceptance conditions and corresponding manufacturing allowance
Project implicationAppropriate when product requirements fit this classNeeds early alignment of design, fabrication and qualification requirements

IPC 6012 class 1 addresses general electronic products and is not a substitute for a required Class 2 build. At the other end, specifying IPC 6012 class 3 does not by itself establish compliance with every medical, automotive or aerospace requirement. Relevant addenda and product-specific obligations can apply. Choosing the class early is more effective than trying to upgrade a completed lot through inspection alone.

How Does IPC-6012 Differ from IPC-A-600 and IPC-A-610?

IPC-6012 defines rigid-board qualification and performance requirements; IPC-A-600 helps interpret printed-board acceptability visually; IPC-A-610 concerns electronic assemblies. These documents address related but different parts of the product, so they are not interchangeable.

A solder joint on a mounted component belongs to the assembly discussion, whereas a plated hole inside the bare board belongs to board fabrication. If your project includes both PCB manufacture and assembly, we can support both stages, but each needs its appropriate acceptance basis. Our IPC-A-600 bare PCB inspection explanation describes how visual and internal observations complement performance requirements.

Does Class 2 Determine Layer Count, Finish or Impedance?

No. Class 2 is not a complete stack-up or electrical design. A board can require controlled impedance, a particular laminate or a specific surface finish in addition to Class 2 acceptance. Those choices come from the circuit and its assembly requirements.

For example, a communications board may need a defined impedance structure, while an industrial control board may place greater emphasis on current capacity and terminal spacing. Both can use a Class 2 acceptance basis without sharing the same construction. We offer FR4 builds up to 32 layers, subject to engineering review. We can discuss the stack-up, routing density and assembly needs together to identify a suitable construction for your design.

Early DFM support helps connect your intended circuit with manufacturable pads, holes and conductor geometry. It also makes special requirements visible before production, rather than leaving them to be inferred from a general class note.

Which IPC-6012 Revision Applies?

The IPC 6012 latest revision listed in the official revision table is IPC-6012F, September 2023, checked on September 11, 2026. The agreed revision for an existing product can differ. The letter identifies the edition; Class 2 identifies a performance level within that edition.

A legacy drawing referring to IPC 6012D class 2 should therefore not be silently treated as a Class 2 callout under revision F. Where your product moves to a newer edition, the affected requirements need to be aligned with the design and manufacturing agreement. Different editions of an IPC-6012 PDF are not interchangeable simply because they discuss the same class.

What Does IPC-6012 Certification Mean?

IPC-6012 certification can refer to different things, including an individual’s training credentials or a manufacturing qualification program with a defined scope. Neither should be confused with the conformity of a particular board lot. The certificate, issuing organization and scope determine what a certification claim actually establishes.

For the PCBs you receive, the useful evidence relates to the agreed board revision, specified class and applicable manufacturing or test records. A company-level quality certificate alone does not replace that product-specific evidence, and a bare-board acceptance result does not prove the completed equipment’s functionality.

How Can We Support Your Class II PCB Project?

We support PCB fabrication, DFM and PCB assembly, helping you carry the intended board requirements from design into a practical build. Our available inspection and test capabilities include microsection preparation and analysis, copper-thickness checks, AOI and flying-probe testing. Tell us which test reports your project needs so we can confirm the test scope and delivery documentation with your build.

Send your board files, fabrication drawing and intended application to sales@bestpcbs.com. At EBest Circuit (Best Technology), we can review your IPC-6012 class II requirements alongside the stack-up, material and assembly needs, so the board specification supports the product you are building.

You may also like

PCB feed-through card: Vias, Connectors and Filters

September 11th, 2026

A PCB feed-through card can carry power or signals between connections in an equipment assembly, with filtering added where the circuit needs noise suppression. Understanding that electrical path makes it easier to distinguish the board itself from its connectors, plated holes and filter components—and to choose a replacement that preserves the original function.

EBest Circuit (Best Technology) combines PCB fabrication and component sourcing with SMT, through-hole and mixed PCB assembly. For a board combining connector pins and small filter components, this means both assembly methods can be handled within the same project. We also support customer-supplied components, giving you the option to retain specified connectors while arranging the remaining procurement and assembly with us. Contact sales@bestpcbs.com to discuss a suitable build option.

PCB feed-through card

What does PCB feed-through card mean?

The phrase is an equipment-specific description: it identifies a board or assembly by its connection function. It does not specify one universal circuit, connector arrangement or pinout. To understand a particular card, distinguish the complete assembly from the features that form its electrical paths.

The board, connection and filter perform different jobs:

  • The card carries the circuit. Its copper tracks establish connections between terminals or other parts of the equipment.
  • Vias connect copper layers. They let a connection continue through the board thickness.
  • Connectors provide the interface. They join the board or equipment to wiring or a mating assembly.
  • Filter components control noise. Where fitted, they change how unwanted high-frequency energy travels through the connection.

Consider a simple pass-through board connecting an incoming cable to an internal circuit. A connector accepts the cable, copper tracks route its connections, and vias move selected tracks between layers. Adding a feed-through filter to a power connection gives that route a noise-suppression function. These features can work together; they are not alternative names for the same object.

The schematic reveals which arrangement a particular card uses: direct connections, filtered connections, or additional circuitry. That distinction explains more about its operation than the word “feed-through” alone.

Feed-through vias vs. component mounting holes

A feed-through via is a plated electrical connection between PCB layers. A component hole receives a physical lead or pin. The difference is easiest to see around a through-hole connector: its pins enter the component holes, while nearby vias connect tracks or ground areas to another copper layer.

Hole typeWhat occupies the hole?What determines its design?
Plated viaNormally no component leadInterlayer routing, plating and electrical requirements
Plated component holeA component lead or connector pinThe component's pin dimensions and attachment method
Non-plated mounting holeA screw, locating feature or empty clearanceMechanical fit and positioning

For a soldered connector pin, the finished hole must accommodate the lead and the intended solder joint. A via has no inserted pin to accommodate, so its dimensions serve the routing and electrical requirements instead. Selecting one hole size for both jobs can therefore compromise connector fit or waste routing space.

On a through-hole circuit board, the manufacturing drawing therefore needs to distinguish component holes, vias and mechanical holes. This prevents a connector's mounting requirements from being mistaken for ordinary routing-hole dimensions.

PCB feed-through card

What does a feed through connector do?

A feed through connector carries an electrical connection across a physical boundary, such as an enclosure wall. It provides a defined point where external wiring meets the equipment inside. Depending on the design, the internal side connects to another cable, terminals or a PCB.

The connector and the PCB solve different parts of the connection. The connector establishes the mating interface; the PCB routes those contacts onward. A panel-mounted feed-through may be supported by the enclosure, while a board-mounted connector depends on its PCB attachment and any additional mechanical supports. The mounting arrangement determines where mating forces are carried.

For a replacement, pin pitch alone is insufficient. Two connectors with the same spacing can have different keying, contact numbering or mating depths. An apparently matching plug can therefore connect the wrong circuits or fail to engage correctly.

An ordinary conductive feed-through passes the intended electrical connection continuously. Insulation separates adjacent contacts or separates them from the housing; galvanic isolation requires a different circuit arrangement. Filtering and sealing are additional functions of specified products, not inherent properties of every feed-through connector.

When are feed through capacitors needed?

Feed through capacitors are useful when high-frequency noise must be reduced along a power or suitable signal path. In a three-terminal feed-through arrangement, current passes through the component's conductive path, while its capacitance provides a path for noise to ground. The low-inductance structure helps it remain effective at frequencies where a conventional capacitor's parasitic inductance limits suppression.

Choose the connection according to the problem being solved:

  • Noise travelling along a power line: A through connection places the filter in that route. The supply trace is interrupted so that current flows through the component's input and output terminals.
  • Local IC supply-voltage fluctuations: A non-through connection uses the component for bypass decoupling while retaining the main supply trace. Because noise can also continue along that trace, it offers less suppression of escaping noise than the through arrangement.
  • A line carrying useful signals: The filter must pass the required signal spectrum. If unwanted noise lies close to useful signal frequencies, indiscriminately adding capacitance can suppress signal harmonics as well as noise. The filter response must suit both.

For a power-line through connection, first eliminate parts that cannot meet the operating voltage and current. Then compare attenuation over the troublesome frequency range and the voltage drop caused by the component's DC resistance.

A simple voltage-drop example: If a candidate filter has 20 mΩ of DC resistance and carries 2 A, its calculated drop is 40 mV:

Voltage drop = current × resistance = 2 A × 0.020 Ω = 0.040 V.

That is an illustrative calculation, not a rating for a particular product. It shows why a filter can have suitable noise performance yet consume too much of a low-voltage rail's available voltage margin. Select for both electrical delivery and noise suppression.

How do PCB layout and grounding affect feed-through filters?

The filter's ground connection is part of the noise-current path. A long, narrow route to ground adds inductance, making that path harder for high-frequency current to follow. Consequently, the same filter can produce different attenuation on two boards.

Three layout choices have a direct effect:

  • Ground-trace length and width: Short, wide connections reduce the inductance added between the filter's ground pads and the grounding structure.
  • Distance to the ground plane: A via reaching a nearby plane has a shorter connection than one reaching a plane near the opposite board surface. Stackup matters even when the top-view layout looks identical.
  • Ground connections at the component: In a multilayer mounting comparison, connecting both ground sides through vias gave greater attenuation than using a single ground-side via; shorter vias also improved performance. These are results for that arrangement, not a universal via-count rule.

Keep the incoming and outgoing routing distinct around the filter as well. Closely coupled input and output structures can allow some high-frequency noise to couple around the component. Both the through/non-through choice and this input/output routing effect determine whether noise actually follows the intended filtering path.

For a multilayer PCB, the practical priority is to establish the ground-plane position and the filter's connection paths together. Changing the ground-layer depth during a board revision can change filtering behavior even if the component and its surface footprint remain unchanged.

What must match when replacing a feed-through card?

A successful replacement preserves how the card connects, fits and behaves in the equipment. Three differences are especially easy to miss when comparing boards by appearance.

Pin mapping can change without changing the connector outline.

Imagine two boards using the same six-position connector. On one, contact 1 carries supply power; on the other, it carries ground. The plug may fit both perfectly, but the boards are electrically incompatible. Connector orientation and contact numbering must therefore be interpreted from the specified viewing direction, not guessed from a photograph.

A filtered connection can look like a simple pass-through.

Replacing a filter with a copper link preserves DC continuity but removes its intended noise suppression. Even a capacitor with the same nominal capacitance may differ in internal construction, resistance or high-frequency response. A replacement should preserve the relevant electrical characteristics, not merely the marking value.

Mechanical fit includes the assembled components.

A board can match the original outline yet place a connector too high, reverse its mating direction or leave insufficient clearance inside the enclosure. Board thickness, mounting-hole positions and connector location need to work as one assembly.

The original assembly part number and revision provide a useful starting point for these comparisons. When reproducing an obsolete board, concentrate first on its connection map, populated components and assembled geometry. Resolve those differences before treating a similar-looking board as interchangeable.

PCB feed-through card

FAQs About PCB feed-through card

Is a multilayer PCB required for a feed-through card?

No. A simple connection board may use a simpler layer structure. Additional layers become useful when routing density, grounding or signal requirements justify them. The term “feed-through” does not specify a layer count.

Can one card combine through-hole connectors and surface-mount filters?

Yes. Connector pins and small filter components can use different mounting methods on the same board. This calls for mixed assembly rather than treating the whole card as exclusively SMT or through-hole.

Will a continuity test verify the card's filtering performance?

No. Continuity checks whether a conductive path exists. Filtering concerns how the circuit behaves across frequency, so it requires a measurement suited to the noise or signal requirement. Both checks can be useful, but they answer different questions.

Can I supply the connectors for a custom build?

Yes. EBest Circuit supports consignment and partial turnkey assembly, allowing you to supply specified components while we arrange the agreed remaining procurement and assembly. This is useful when a connector must match existing equipment or cable assemblies.

Should I order a bare PCB or an assembled card?

Order a bare PCB when you will install the connectors and other components yourself. Order an assembled card when you need those components fitted. A bare board reproduces the copper and hole structure; the populated components complete the specified circuit.

Planning a custom PCB feed-through card for your equipment? EBest Circuit can manufacture the board and assemble its specified connectors and components, including mixed SMT and through-hole builds. Email sales@bestpcbs.com to discuss turning your board design into an assembled unit ready for your equipment trials.

You may also like

PCB and PCBA manufacturer USA: Compare Your Options

September 10th, 2026

For a PCB and PCBA manufacturer USA buyers can work with directly, options include Sierra Circuits, Gorilla Circuits, and Cirexx. These companies offer domestic fabrication and assembly, with services covering standard FR4 prototypes, complex multilayer boards, and specialized constructions. Small-order availability and HDI capability help distinguish the services within that market.

For projects that allow overseas production, EBest Circuit (Best Technology) combines PCB manufacturing, component sourcing, and assembly in China. Our capabilities include FR4 boards up to 32 layers and BGA assembly down to 0.25 mm pitch, supporting projects from bare-board prototypes to populated assemblies. Discuss your US project with our team at sales@bestpcbs.com, or arrange a factory visit to see our manufacturing operations firsthand.

PCB and PCBA manufacturer USA

US PCB Manufacturers Offering Fabrication and Assembly

Sierra Circuits, Gorilla Circuits, and Cirexx each provide both PCB fabrication and assembly. Their service ranges cover different board technologies and production needs.

Manufacturer PCB manufacturing Assembly services
Sierra Circuits Standard rigid FR4 and custom advanced boards, including HDI In-house assembly and component procurement
Gorilla Circuits Multilayer boards, hybrid constructions, and semiconductor test boards In-house assembly, parts procurement, and testing options
Cirexx Rigid, flex, rigid-flex, HDI, and RF/microwave boards Turnkey, partial turnkey, and consignment assembly

Sierra Circuits offers a defined route for conventional prototypes through Turnkey PRO, which combines rigid-board fabrication, parts, and assembly. More complex constructions use its custom services.

Gorilla Circuits fabricates and assembles boards at its San Jose, California campus. Its semiconductor test work includes final-test and probe-card boards, making this a relevant area of experience for buyers sourcing complex test hardware.

Cirexx combines fabrication and assembly within the same facility. Flex and rigid-flex assembly are particular areas of specialization, alongside rigid-board and HDI work.

Do All PCB Manufacturers Offer Assembly?

No. A PCB fabrication order normally supplies bare boards; assembly adds the components. Some manufacturers provide both services, while others specialize in one stage.

  • PCB fabrication: bare boards ready for component assembly.
  • Consignment assembly: assembled boards using customer-supplied materials.
  • Full turnkey PCB assembly: fabrication, component purchasing, and assembly managed by the supplier.

An assembler can also purchase bare boards from a fabrication partner. Consequently, turnkey service does not necessarily mean both processes happen in the same factory.

If you already have an assembly partner, a specialist bare-board manufacturer may fit your project well. If you need finished assemblies and want one point of coordination, a fabrication-and-assembly provider can handle the transition between the two stages.

US Manufacturing vs. Overseas Supply to the USA

US production offers proximity; overseas production broadens the manufacturing options available to US buyers. The balance changes with the way a project is developed and ordered.

Consideration US manufacturing Overseas supply to the USA
Factory access Easier domestic visits and sample exchanges Visits require international travel
Engineering communication Greater overlap with US working hours Responses span different working hours
Shipping Domestic transport to the customer International transit before US delivery
Repeat orders Convenient for closely coordinated local production Can suit scheduled orders with planned shipping

During active development, proximity can be valuable. A team making frequent revisions may benefit from easier sample exchanges and direct factory interaction. The relevant schedule is the complete cycle from placing a build to evaluating the hardware.

For a stable design, manufacturing fit becomes more prominent. Materials, copper construction, component availability, and the supplier's ability to repeat the build can matter more than how often the team can visit. Overseas production is worth considering when international transport fits that schedule.

Neither location guarantees a lower total price. Compare equivalent finished boards: the same materials, components, assembly scope, and delivery destination. A bare-board quotation and a complete PCBA quotation cover different purchases.

Which US PCB and PCBA Manufacturers Accept Small Orders?

Sierra Circuits, Cirexx, and PCB Unlimited offer services for prototype or low-volume assembly. Their small-order arrangements differ:

Provider Small-order service Relevant option
Sierra Circuits Turnkey PRO: generally 2–100 assembled boards, depending on the design Standard rigid FR4 turnkey builds
Cirexx High-mix, low-quantity assembly; prototype through medium volume Custom rigid, flex, and rigid-flex projects
PCB Unlimited USA assembly service with no minimum order quantity Turnkey or customer-supplied-material assembly

PCB Unlimited offers US assembly services. Sierra and Cirexx also provide in-house board fabrication. For Sierra, confirm availability before planning a one-board assembled order.

A small quantity can still involve a custom board. A five-board rigid-flex project or a four-layer PCB with a specified stackup may need a custom service rather than a standard prototype package.

Small runs also share production preparation across fewer finished boards. Stencil preparation and machine programming are needed even for a short run, so doubling the assembled quantity does not necessarily double the total price. When several engineers need hardware simultaneously, pricing the actual number of working samples can be more useful than starting with the smallest possible order.

PCB and PCBA manufacturer USA

Which US Manufacturers Offer HDI PCB Fabrication and Assembly?

Sierra Circuits and Cirexx offer both HDI fabrication and assembly. Their capabilities include the board interconnections and component assembly needed for dense designs.

Manufacturer HDI fabrication Assembly support
Sierra Circuits Custom HDI boards with advanced via structures Turnkey HDI assembly with component sourcing
Cirexx Laser-drilled microvias, blind/buried vias, sequential lamination, and via-in-pad Double-sided HDI SMT/BGA assembly

Sierra's HDI projects use its custom manufacturing route. The standard Turnkey PRO package excludes HDI and multiple laminations, so it is a separate service from the company's advanced-board offering.

Cirexx combines HDI fabrication with dense assembly work. Its fabrication processes include laser direct imaging and controlled-depth drilling, while its assembly service covers double-sided SMT/BGA builds and flex or rigid-flex boards.

For a compact BGA board, this combination is important: the fine-pitch package must be supported by a manufacturable routing and via structure beneath it. Choosing a supplier that handles both allows those fabrication and assembly requirements to be addressed together.

PCB and PCBA manufacturer USA

How EBest Circuit Supports US PCB and PCBA Buyers

With EBest Circuit, US customers can source bare PCBs, populated boards, or a complete turnkey build through one manufacturing partner. Our PCB manufacturing capabilities cover conventional FR4 and more demanding multilayer constructions.

Capability EBest Circuit support
FR4 layer count Up to 32 layers
HDI trace width/spacing Down to 2/2 mil
Small-component assembly Down to 01005
BGA assembly Down to 0.25 mm pitch
Assembly methods SMT, through-hole, and mixed assembly

The applicable combination depends on the board construction and component layout.

Keep component purchasing flexible. Our PCB assembly services include full turnkey, partial turnkey, and consignment work. You can use components already held by your team while we source the remaining parts, or have procurement included with the build.

Combine fine-pitch assembly with solder-joint inspection. Fine-pitch placement supports compact layouts, while AOI and X-ray inspection provide complementary checks for visible features and hidden solder joints.

Plan prototype and repeat builds with clear timing. Standard PCBA service is approximately one week, with expedited options for eligible projects. Our production lead times distinguish PCB fabrication from assembly; component procurement and delivery to the USA also need to fit the overall schedule.

Case Study: A 4-Layer Medical PCB for a US Customer

EBest Circuit worked with a US customer on a four-layer FR4 PCB for a medical product. The project required TG170 material, a finished thickness of 1.6764 mm ±10%, and 2 oz finished copper on every layer. The customer's PDF defined the layer structure.

Three requirements gave this board its specific manufacturing character:

  • The same finished copper requirement on all four layers. Both inner and outer layers required 2 oz copper. An outer-layer-only 2 oz specification would not describe this board correctly, and the customer's stackup formed part of the required construction.
  • Copper retention around non-plated holes. Where a pad was larger than an NPTH, the customer required its position and copper to remain unchanged. Secondary drilling was specified to produce the hole without treating the surrounding pad copper as material to remove.
  • A defined PTH copper requirement. Minimum hole-wall copper had to follow IPC-6012 Class 3 requirements. This was a distinct requirement from the 2 oz finished copper specified for the circuit layers.

The board also required lead-free HASL, glossy green solder mask on the top side, and white silkscreen clear of the pads. Routed internal corners had to follow the maximum radii on the drawing.

FAQs About PCB and PCBA manufacturer USA

Can a US assembly company work with overseas-manufactured PCBs?

Yes, if it accepts customer-supplied boards or sources them through a fabrication partner. This arrangement lets you retain a bare-board supplier while assembling closer to your US team.

Can prototype orders use a custom stackup?

Yes. Small quantity and custom construction can be combined. The order needs a service that accepts the specified stackup rather than a package limited to the supplier's standard constructions.

Can I provide some components and have the supplier purchase the rest?

Yes. Partial turnkey assembly supports this arrangement. It is useful when you already hold selected devices but want the manufacturer to procure the remaining components.

Does PCB electrical testing replace PCBA functional testing?

No. Bare-board electrical testing checks circuit connectivity before assembly. Functional testing evaluates the populated board against its intended functions and requires an appropriate test method.

Can EBest Circuit support a US project from bare boards through assembly?

Yes. EBest Circuit provides PCB fabrication, component sourcing, and assembly in China for US customers. The project can be supplied as bare boards or developed into a turnkey assembly order.

Discuss your next PCB or PCBA project with EBest Circuit at sales@bestpcbs.com. If you would like to meet the team and see our production operations before choosing a manufacturing partner, we welcome you to arrange a factory visit. PCB and PCBA manufacturer USA

You may also like

Cleaning Electronics With Rubbing Alcohol: 70%, 90%, or 99% IPA?

September 10th, 2026

Cleaning electronics with rubbing alcohol can be safe when the device is disconnected from power, the liquid is kept out of openings, and the concentration matches the surface. For exposed PCBs, 90% to 99% electronics-grade isopropyl alcohol (IPA) is usually a better starting point than 70% rubbing alcohol because it contains less water and dries faster.

That does not make IPA a universal electronics cleaner. Display coatings, printed legends, adhesives, unsealed sensors, and some plastics may be damaged. The contamination also matters: IPA can lift oils and many rosin-based flux residues, but it may not remove salts, sugary spills, water-soluble flux, or cured residues.

Technician cleaning a powered-off PCB at an ESD-safe workbench with rubbing alcohol

Can You Clean Electronics With Rubbing Alcohol?

Yes, you can clean selected electronics with rubbing alcohol after removing power and confirming that the device maker permits alcohol on the target surface. A slightly damp lint-free cloth may be suitable for an approved hard exterior, while an exposed PCB normally calls for controlled application of 90% to 99% electronics-grade IPA.

First decide which job you are doing:

  • Exterior wiping: Some manufacturers permit 70% IPA wipes on hard, nonporous surfaces. Apple and Dell publish product-specific examples, but their instructions do not apply automatically to every device.
  • Exposed-board cleaning: Repair guides commonly use at least 90% IPA for localized work on a disconnected logic board or PCB.
  • Disinfection: The concentration and wet contact time needed to disinfect a surface are different from the requirements for removing flux or oil from a circuit board.

Never spray alcohol directly onto a device. Wet the cloth, foam swab, polyester swab, or ESD-safe brush away from the electronics, then apply only enough liquid to loosen the soil.

Is Rubbing Alcohol Safe for Electronics?

Rubbing alcohol is safe only for compatible materials and controlled, unpowered cleaning; it is not safe to pour into an assembled device or use around ignition sources. A 70% IPA wipe may be approved for a laptop shell or keyboard, yet the same liquid can enter a connector, remain beneath a shield, soften adhesive, or mark a coated display.

This is why the answer to whether rubbing alcohol is safe for electronics depends on the exact part, contamination, and application method rather than the device category alone.

The label matters as much as the percentage. A bottle sold as first-aid rubbing alcohol is formulated for topical use, not residue-sensitive PCB production. Many 70% products contain 30% water, and formulations vary by supplier. Before use, check the active ingredients, inactive ingredients, and safety data rather than assuming every clear alcohol product is equivalent.

IPA is also highly flammable. NIOSH lists isopropyl alcohol as a Class IB flammable liquid with a 53°F (12°C) flash point. Keep it away from soldering irons, hot-air rework tools, sparks, smoking, and open flame; cap the container when not in use and provide ventilation.

What Percentage Isopropyl Alcohol for Electronics?

Use the device maker’s approved product for finished equipment; for localized exposed-PCB cleaning, 90% to 99% electronics-grade IPA is the practical starting range because it contains only 1% to 10% water instead of the 30% found in 70% IPA. Higher purity does not override component, coating, or adhesive restrictions.

IPA Concentration Approximate Water Content Suitable Starting Use Main Limitation
70% 30% Approved hard exterior surfaces using a damp wipe Slower drying and more water; not the default for exposed PCBs
90% or 91% 9% to 10% Localized PCB repair and residue removal when compatible Can still affect coatings, plastics, markings, and adhesives
99% or 99.9% 0.1% to 1% Moisture-sensitive, residue-controlled bench cleaning Still flammable and not effective against every contaminant
Comparison of 70 percent, 90 percent, and 99 percent IPA for exterior and exposed PCB cleaning

Do not dilute high-purity IPA with tap water for PCB work. Tap water can add minerals and ions. If an aqueous process is required, it should use chemistry, rinse-water quality, and drying conditions chosen for the assembly.

What Is the Difference Between Rubbing Alcohol and Electronics-Grade IPA?

Household rubbing alcohol is usually sold as a skin antiseptic, whereas electronics-grade IPA is supplied with controlled purity and residue expectations for cleaning components and assemblies. A common 70% first-aid product is 70 mL IPA per 100 mL with water as the inactive ingredient; an electronics cleaner may be 99.9% anhydrous IPA with a technical data sheet and safety data sheet.

Do not judge a cleaner by the front label alone. Check:

  • IPA concentration and water content;
  • listed fragrance, dye, oil, bitterant, or other additive;
  • nonvolatile residue specification, if provided;
  • plastics, elastomer, coating, and adhesive compatibility;
  • storage, ventilation, and personal-protection instructions in the SDS.

For a repeatable manufacturing process, lot-controlled cleaner and documented compatibility are more useful than a generic pharmacy bottle whose intended use is first aid.

Which Parts Should Not Be Cleaned With Rubbing Alcohol?

Do not apply rubbing alcohol to an unapproved display coating, printed key legend, foam adhesive, acrylic or polycarbonate part, unsealed microphone, speaker, sensor, relay, or coated PCB area without a material check. Even when the bare laminate and solder mask tolerate IPA, a complete assembly may contain liquid-trapping or solvent-sensitive parts.

Display coating, printed legends, adhesive tape, and an unsealed sensor that require IPA compatibility checks
  • Displays and lenses: Alcohol can affect oleophobic, anti-glare, or other surface treatments unless the manufacturer permits it.
  • Printed markings: Repeated wiping can fade legends on keys, component bodies, labels, and enclosures.
  • Adhesives and foam: IPA is often used to weaken adhesive during repair, which is exactly why it must be controlled near display seals, battery tape, gaskets, and foam pads.
  • Liquid-sensitive devices: Microphones, speakers, MEMS parts, unsealed switches, relays, transformers, and trimmers can trap solvent or suffer mechanical damage.
  • Conformal coating: Cleaning a coated board and intentionally removing coating are different processes. Review the coating chemistry before applying solvent.

How Should You Prepare Electronics Before Cleaning?

Shut the device down, unplug every cable, remove the battery when serviceable, verify stored energy is discharged, and move the work away from sparks, hot tools, and open flame. A power button does not isolate every energy source, and power supplies or large capacitors may retain hazardous voltage after unplugging.

  1. Read the product cleaning or service instructions.
  2. Photograph connectors, cable routing, corrosion, and residue before disassembly.
  3. Disconnect mains power, external supplies, and batteries.
  4. Use an ESD-safe mat, grounded tools, and an ESD-safe brush for sensitive boards.
  5. Remove loose dust first so wet cleaning does not turn it into a paste.
  6. Test the cleaner on a hidden or representative material when compatibility is uncertain.
  7. Use ventilation and keep the IPA container away from ignition sources.

If you cannot safely discharge the equipment, access the board without damaging seals, or identify a swollen battery, stop and use a qualified repair service.

How Do You Clean an Exposed PCB With Isopropyl Alcohol?

Apply a small amount of 90% to 99% electronics-grade IPA to a low-lint swab or ESD-safe brush, loosen the soil, then lift the dissolved residue with clean material instead of letting dirty solvent dry on the board. The goal is removal, not simply spreading a dissolved film across a larger area.

Controlled cleaning of flux residue from an exposed PCB with a low-lint swab
  1. Inspect and classify the soil. Note whether it is dry dust, oil, flux, drink residue, corrosion, or an unknown deposit.
  2. Remove dry particles. Use an ESD-safe soft brush or controlled clean air without forcing debris under packages.
  3. Dampen the tool. Add IPA to the swab or brush away from the PCB; do not pour from the bottle onto the board.
  4. Agitate gently. Work around solder joints and leads without bending parts or snagging fine wires.
  5. Lift the dissolved residue. Blot with a clean low-lint wipe or use fresh solvent as a controlled final rinse.
  6. Replace dirty materials. A brown swab or cloudy solvent is carrying contamination and should not be reused for the final pass.
  7. Dry, inspect, and test. Confirm that connectors, shields, sockets, and package gaps are dry before reconnecting power.

For a broader method covering dust, corrosion, coating, and aqueous cleaning, see our guide to cleaning a PCB board safely.

Which Contaminants Need More Than IPA?

Salt, sugary drinks, water-soluble flux, corrosion products, and unknown deposits may require a qualified aqueous rinse, flux-specific cleaner, or repair process rather than an IPA-only wipe. IPA can evaporate while nonvolatile ionic contamination stays behind.

Contaminant Suitable Starting Method Why IPA Alone May Fail
Finger oil or light grease Compatible high-purity IPA and clean low-lint material Dirty solvent can redeposit an oily film
Rosin-based flux High-purity IPA or matched flux remover after compatibility check Heat-aged or polymerized residue may resist IPA
Water-soluble flux Validated aqueous chemistry and DI-water rinse IPA may not remove the ionic activator system
Sugary or salty spill Controlled aqueous cleaning, DI rinse, and complete drying when parts allow Alcohol can leave conductive nonvolatile material behind
Corrosion Cleaning plus magnified damage assessment and repair Solvent cannot restore missing copper or damaged terminations

Flux chemistry should be identified before selecting the cleaner. Our explanation of flux residue and cleaning methods shows why water-soluble, rosin, and no-clean materials cannot share one blanket instruction.

In our PCBA projects, we treat cleaner selection, rinse quality, drying, and inspection as one process. Changing only the solvent can leave the same ionic residue or hidden moisture problem in a different form.

How Long Should Electronics Dry Before Power-On?

Do not use one universal minute count; restore power only after visible liquid and alcohol odor are gone and no fluid remains trapped under shields, connectors, sockets, switches, or packages. A lightly wiped open surface may appear dry within minutes, while a flooded connector or shielded area can retain solvent much longer.

Use these release checks:

  • no droplets, wet sheen, or cleaner line visible under magnification;
  • no liquid emerging when the board is tilted or gently repositioned;
  • connectors and sockets inspected from more than one angle;
  • no alcohol odor at close range in a ventilated area;
  • no residue film, displaced component, lifted pad, or damaged marking;
  • the device maker’s minimum drying instruction has been met.

Do not use a hot heat gun to accelerate drying. Excessive heat can deform connectors, soften adhesives, damage batteries, or stress solder joints. Use clean dry air or a controlled low-temperature process only when the component limits are known.

What Mistakes Damage Electronics During Alcohol Cleaning?

The highest-risk mistakes are cleaning an energized device, spraying directly into openings, flooding liquid-sensitive parts, using a contaminated swab, and restoring power before trapped solvent has evaporated. Most failures come from uncontrolled application or wrong-material use, not from the word “alcohol” alone.

  • Using 70% as the universal choice: It may be suitable for an approved exterior but adds more water to an exposed assembly.
  • Using a soaked cotton swab: Excess liquid can wick under components, and loose fibers can snag on leads.
  • Letting dirty IPA evaporate: Dissolved flux and oil remain unless they are lifted or rinsed away.
  • Scrubbing harder: Force can remove markings, dislodge 0201/01005 components, bend contacts, or break corroded leads.
  • Ignoring the original fault: Cleaning cannot repair a cracked joint, missing copper, swollen battery, or internally corroded component.
  • Applying conformal coating over residue: Cleanliness and dryness must be verified before coating, or contamination may be sealed onto the assembly.

Production control begins earlier than final cleaning. For example, solder paste inspection in PCB assembly can catch printing defects before placement and reflow, while post-solder cleaning addresses only the residue left by the selected materials and process.

FAQ About Cleaning Electronics With Rubbing Alcohol

These answers cover the most common concentration, surface, flux, and power-on questions about using rubbing alcohol on electronics.

Can I use 70% rubbing alcohol on a circuit board?

Use 70% rubbing alcohol on an exposed circuit board only when the assembly documentation permits it and no better high-purity option is available. Its 30% water content slows drying and raises the chance of liquid remaining in gaps. For localized exposed-PCB cleaning, 90% to 99% electronics-grade IPA is usually the safer starting range.

Is 91% rubbing alcohol good for electronics?

91% IPA is suitable for many localized PCB-repair tasks because it contains about 9% water and evaporates faster than 70%. It can still soften adhesive, affect markings, or enter unsealed parts, so apply a small amount to a low-lint tool and check material compatibility first.

Can I use 99% isopropyl alcohol on a phone screen?

Do not use 99% IPA on a phone screen unless the phone manufacturer explicitly approves it for that model and surface. Screen coatings and display seals vary. Many device makers specify a slightly damp lint-free cloth or a 70% IPA wipe for selected exterior surfaces, not unrestricted use of 99% liquid.

Does isopropyl alcohol remove solder flux?

IPA removes many fresh rosin-based flux residues, especially at 91% to 99%, but it does not remove every no-clean or heat-aged residue. Water-soluble flux normally requires a validated aqueous process. Match the cleaner to the exact flux product and remove the dissolved soil rather than letting it dry on the PCB.

Can cleaning electronics with alcohol cause a short circuit?

Cleaning electronics with alcohol can cause a short circuit if power is present, the liquid contains conductive contamination, or water and dissolved residue remain trapped when the device is energized. Disconnect every power source, control the liquid, dry hidden areas, inspect the board, and only then perform a safe functional test.

Can I pour rubbing alcohol over a motherboard?

Do not pour household rubbing alcohol over an assembled motherboard. Flooding carries dirt beneath packages and into connectors, fans, sockets, microphones, switches, or other liquid-sensitive parts. Board immersion is a specialized repair process that requires disassembly, compatible components, suitable high-purity solvent, ventilation, and controlled drying.

How Can EBest Circuit Support Cleaner, More Reliable PCB Assemblies?

We match the cleaning method to the flux, component set, coating plan, inspection requirement, and end-use risk instead of treating IPA as a universal production solution. At EBest Circuit, we support PCB fabrication, component sourcing, PCB assembly, and inspection within one coordinated project.

For a cleaning-sensitive assembly, send us the Gerber files, BOM, placement data, assembly drawing, target flux or solder-paste specification, coating requirement, quantity, and cleanliness or test criteria. We can review the build information before production and align the inspection plan with the assembly design.

To discuss a PCB or PCBA project, visit our PCB and PCBA manufacturing service page or email sales@bestpcbs.com.

You may also like

What Does Solder Flux Do? How It Works in Electronics Soldering

September 9th, 2026

What does solder flux do? Solder flux removes surface oxides, limits new oxidation during heating, and helps molten solder wet copper pads, component leads, wires, and terminals. Without enough flux activity, solder may bead up or pull away from the metal instead of forming a clean joint.

In electronics soldering, flux may come from flux-core wire, solder paste, liquid flux, or tacky flux used during rework. The chemistry varies by process, but the purpose is the same: keep the soldering surface clean enough for solder to spread and bond while the joint is hot.

What solder flux does during electronics soldering on a PCB

What Does Solder Flux Actually Do?

Solder flux mainly cleans and protects the metal surface so molten solder can wet it properly.

Its main functions are:

  • Remove oxides: Activators react with oxide films on copper pads and component terminals.
  • Limit re-oxidation: Flux temporarily protects hot metal from further exposure to oxygen.
  • Improve wetting: Molten solder can spread across clean metal instead of remaining in rounded beads.
  • Support joint formation: Better wetting helps solder make continuous contact with both surfaces being joined.

This is why adding suitable flux can improve a stubborn solder joint even when the soldering temperature is already high enough.

Flux itself is not an adhesive. It prepares the surface so solder can form the actual electrical and mechanical connection.

How Does Solder Flux Work During Soldering?

Solder flux works by becoming chemically active as the joint heats up, removing surface oxides before molten solder reaches the metal.

Five-step diagram showing how solder flux removes oxide and improves solder wetting

A typical sequence is:

  1. Copper pads or component leads have a thin oxide layer.
  2. Flux is applied or released from solder wire or solder paste.
  3. Heat activates the flux.
  4. Flux chemistry reacts with the oxide layer.
  5. Cleaner metal is exposed.
  6. Molten solder wets and spreads across the surface.
  7. The solder cools and forms the joint.

The most important result is better wetting.

Good wetting produces smooth contact between the solder and the metal surface. Poor wetting can leave:

  • rounded solder beads
  • incomplete pad coverage
  • uneven fillets
  • solder that pulls away from the pad or lead

Increasing iron temperature alone does not fix an oxide problem. Excessive heat can accelerate oxidation while also increasing the risk of pad damage or component stress.

Do You Need Flux to Solder?

Yes, most soldering processes need flux activity, but you do not always need to apply flux separately.

Flux-core wire, solder paste, and extra flux used for PCB rework

Flux may already be present in:

  • flux-core solder wire
  • SMT solder paste
  • some solder preforms
  • certain specialty solder products

Extra flux is more useful when the existing flux is no longer sufficient, such as during:

  • PCB rework
  • repeated heating of an old solder joint
  • soldering oxidized pads or leads
  • drag soldering
  • fine-pitch IC soldering
  • BGA or QFN rework

So, if you are using flux-core solder or solder paste, the process already includes flux. Separate flux is only needed when additional oxide removal or wetting support is required.

In production PCBA, flux choice is more than a soldering consumable decision. It can affect solder wetting, residue control, ionic cleanliness, conformal coating compatibility, inspection results, and long-term reliability. For SMT, wave soldering, selective soldering, or rework projects, EBest Circuit can review flux and soldering process requirements together with the PCB design, BOM, and assembly conditions.

Does Solder Already Have Flux in It?

Some solder contains flux, while other solder products do not.

Comparison of solid solder wire, flux-core solder wire, solder paste, and solder bar
Solder Material Contains Flux? Typical Use
Solid solder wire No Controlled or specialized soldering
Flux-core solder wire Yes Hand soldering and repair
SMT solder paste Yes Reflow assembly
Solder bar Usually no Wave and selective soldering
Solder preform Depends on product Specialized assembly

Flux-core solder wire is common in manual electronics soldering. When the wire melts, the internal flux is released directly into the joint.

Solder paste also contains flux, but in a different form. It combines fine solder alloy powder with a flux system designed for stencil printing and reflow.
Extra flux may still help when:

  • the original flux has already been consumed
  • the joint has been reheated several times
  • the surface is oxidized
  • additional wetting is needed around fine-pitch leads

What Does Solder Flux Contain?

Solder flux usually contains a base material, activators, and a carrier or solvent.

The main ingredients are:

  • Base or resin: Often rosin or synthetic resin. It provides the main flux medium.
  • Activators: React with metal oxides during heating.
  • Solvent or carrier: Helps liquid flux spread and evaporates as the assembly heats.

Depending on the product, manufacturers may also add:

  • wetting agents
  • corrosion inhibitors
  • stabilizers
  • rheology modifiers
  • thixotropic agents

The exact formulation affects flux activity, residue, storage stability, application method, and cleaning requirements.

What Types of Flux Are Used in Electronics Soldering?

The main flux types used in electronics are rosin-based, no-clean, and water-soluble flux.

Rosin RMA, no-clean, and water-soluble flux types used in electronics soldering
Flux Type Activity Cleaning Typical Use
Rosin / RMA Low to medium Depends on formulation Hand soldering, repair
No-clean Low to medium Often not required SMT, reflow, wave soldering
Water-soluble Medium to high Normally required More difficult solderability conditions

Rosin and RMA flux

Rosin flux is widely used in electronics. RMA, or mildly activated rosin, adds more oxide-removal capability while remaining suitable for many PCB applications.

No-clean flux

No-clean flux leaves a relatively small amount of residue after soldering and is common in production assembly.

The term “no-clean” does not mean the board is residue-free. It means the remaining residue is designed to stay on the board when the process and product requirements allow it.

Water-soluble flux

Water-soluble flux offers higher activity and can handle more difficult oxidation. Its residues normally need to be removed after soldering.

For PCB work, plumbing or highly acidic flux should not be used because the residue may be too corrosive for electronic assemblies.

Liquid Flux vs Paste Flux: What Is the Difference?

Liquid flux spreads easily, while paste or tacky flux stays in place more effectively.

Flux Form Main Characteristic Typical Use
Liquid flux Low viscosity, spreads easily Wave soldering, selective soldering, repair
Flux pen Controlled liquid application PCB touch-up
Gel / tacky flux Stays around the joint SMD, BGA and QFN rework
Paste-type flux Thick, localized application Hand soldering and rework

Liquid flux is useful when the material needs to flow into narrow spaces or across multiple leads.

Tacky and gel fluxes are more useful during rework because they remain around the component instead of immediately spreading across the board.

Flux paste is not the same as solder paste. Flux paste contains flux chemistry, while solder paste contains both solder alloy powder and flux.

Which Flux Is Best for Soldering Electronics?

The best flux for soldering electronics depends on the soldering process, surface condition, residue requirement, and cleaning method.

Application Typical Flux Choice
General PCB hand soldering Rosin/RMA or electronics-grade no-clean
Fine-pitch IC soldering Liquid or tacky flux
SMT reflow Flux system already contained in solder paste
Wave soldering Process-specific liquid flux
BGA/QFN rework Tacky or gel flux
Oxidized surfaces Higher-activity flux with suitable cleaning

Also check:

  • solder alloy compatibility
  • PCB surface finish
  • flux activity level
  • residue limits
  • cleaning capability
  • conformal coating requirements
  • product reliability requirements

A more active flux is not automatically better. Higher activity may improve oxide removal, but it can also increase cleaning requirements.

Does Flux Need to Be Cleaned After Soldering?

Flux residue should be cleaned when the chemistry or assembly requirements make residue unacceptable.

PCB flux residue cleaning guide for water-soluble, highly active, and no-clean flux

Typical guidance is:

  • Water-soluble flux: Normally clean after soldering.
  • Highly activated flux: Usually clean unless the product specification states otherwise.
  • No-clean flux: May remain if the process and reliability requirements allow it.

Cleaning deserves extra attention for:

  • high-voltage assemblies
  • high-impedance circuits
  • assemblies receiving conformal coating
  • products exposed to high humidity
  • assemblies with strict ionic cleanliness limits

Using too much flux can also leave unnecessary residue, especially during hand soldering and repair. Applying only the amount needed for proper wetting usually gives a cleaner and more repeatable result.

FAQ About Solder Flux

1. What happens if you solder without flux?

Without enough flux, surface oxides can prevent solder from wetting properly. The solder may bead up, form incomplete fillets, or fail to bond evenly to the pad or component lead.

2. Can you use too much flux when soldering?

Yes. Too much flux can leave heavy residue, spread contamination across the PCB, and increase cleaning or inspection work. Use enough to support wetting without flooding the area.

3. Does flux make solder stick better?

Yes, indirectly. Flux removes oxides and improves wetting, allowing molten solder to bond more effectively with the metal surface. Flux itself is not an adhesive.

4. Can you use plumbing flux for electronics soldering?

No. Plumbing flux can be too aggressive or corrosive for PCB assemblies. Use flux specifically formulated for electronics.

5. Why does solder bead up even when I use flux?

Common causes include severe oxidation, contamination, insufficient heat, weak or expired flux, or poor solderability of the surface finish.

6. Do you need extra flux with flux-core solder?

Not always. Flux-core solder already contains flux. Extra flux is mainly useful for rework, oxidized surfaces, fine-pitch soldering, or joints that have already been heated.

Solder flux plays a simple but important role in electronics assembly: it keeps the soldering surface clean enough for molten solder to wet and form a reliable joint.

If you are preparing a PCB or PCBA project and need support with soldering process requirements, assembly manufacturability, or production planning, send your Gerber files, BOM, and assembly requirements to sales@bestpcbs.com

You may also like