PCB manufacturing PCB manufacturing
Home > Blog

selective wave soldering

Selective Soldering Process: How Each Stage Controls Joint Quality
Tuesday, October 6th, 2026

The selective soldering process creates through-hole solder joints only at programmed locations on a PCB assembly. It is commonly used after SMT reflow when connectors, relays, transformers, terminals, switches, or other plated through-hole components still need to be soldered without exposing the entire underside of the board to a full solder wave.

Its advantage is control, but localized soldering does not automatically guarantee good joints. Flux placement, preheat, nozzle condition, solder contact, travel direction, withdrawal, PCB thermal mass, and inspection must work as one connected process. A setting that produces complete barrel fill on a plane-connected power pin may overheat a nearby low-mass joint. A nozzle path that works on an open connector row may bridge pins when an adjacent component changes the solder flow.

This guide explains how each stage works, which variables change the result, and how a stable selective soldering process turns mixed SMT and through-hole assemblies into repeatable production builds.
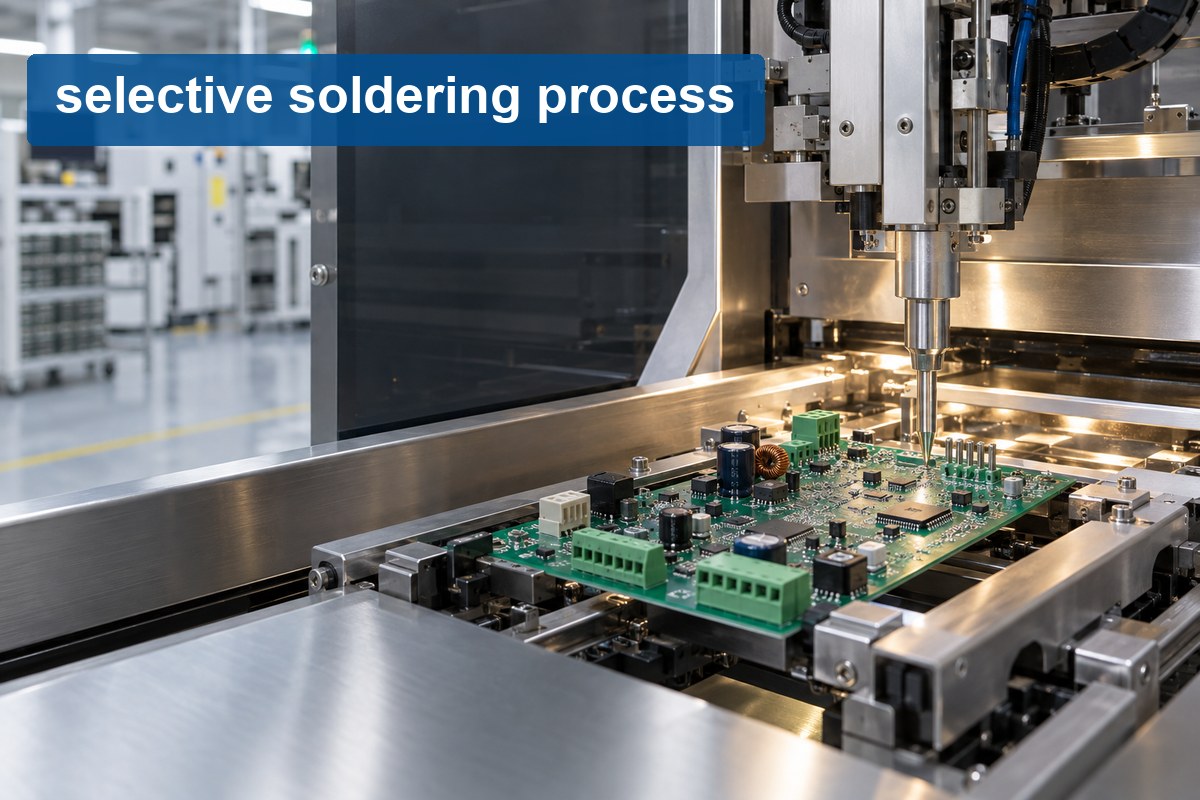
selective soldering process

What Is the Selective Soldering Process?

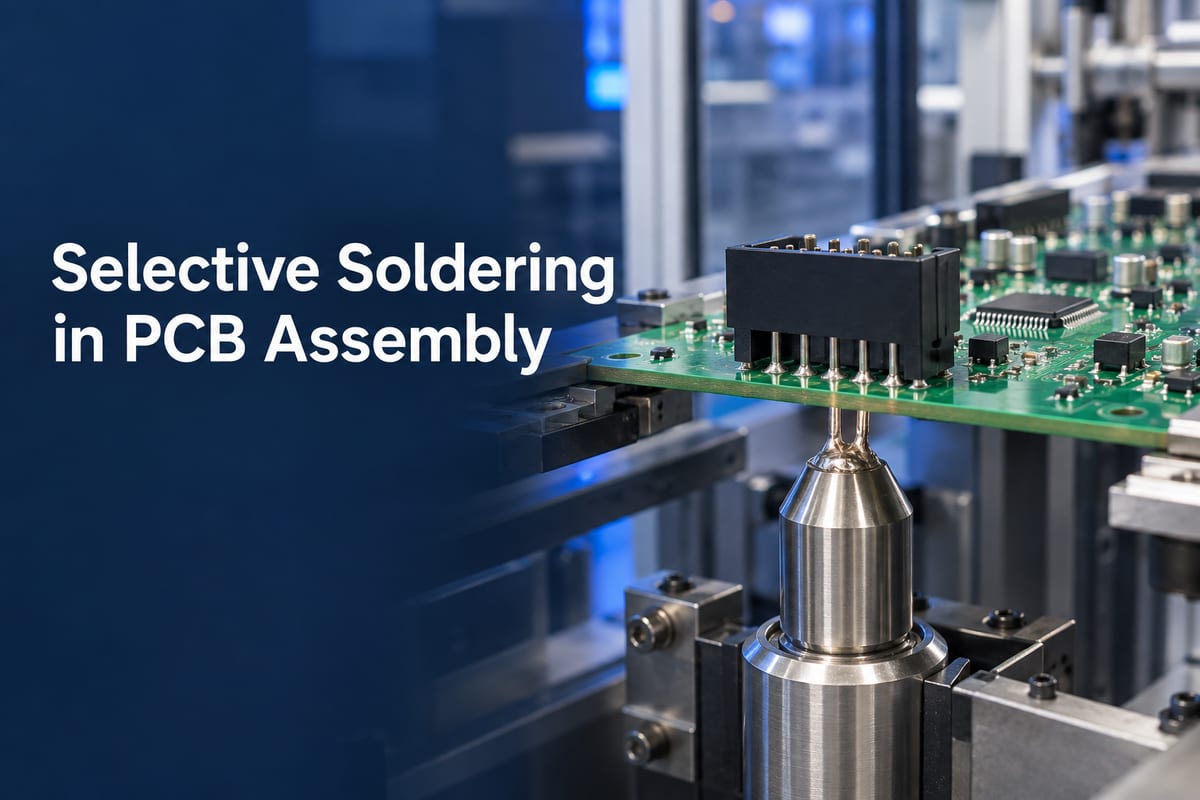
Selective soldering is an automated through-hole assembly process that delivers flux, heat, and molten solder to chosen joints instead of treating the entire PCB underside. A programmed system moves either the PCB or a small solder nozzle so that the solder fountain reaches the required pins while avoiding nearby areas.

The method is especially useful after one or both PCB sides have already passed through SMT reflow. Bottom-side resistors, capacitors, ICs, or other packages may sit close to the remaining through-hole pins. Full wave soldering could require a protective pallet or expose too much of the assembly to heat, while extensive hand soldering may add operator variation. Selective soldering in PCB assembly gives the assembler a repeatable route to the remaining joints when the layout provides sufficient access.

The process is not simply a smaller version of wave soldering. Each target receives its own controlled flux pattern and thermal history. The machine program must account for connector geometry, pin spacing, component mass, copper distribution, board thickness, solder alloy, surface finish, and the location of nearby components.

Selective Soldering Process Steps from Fluxing to Inspection

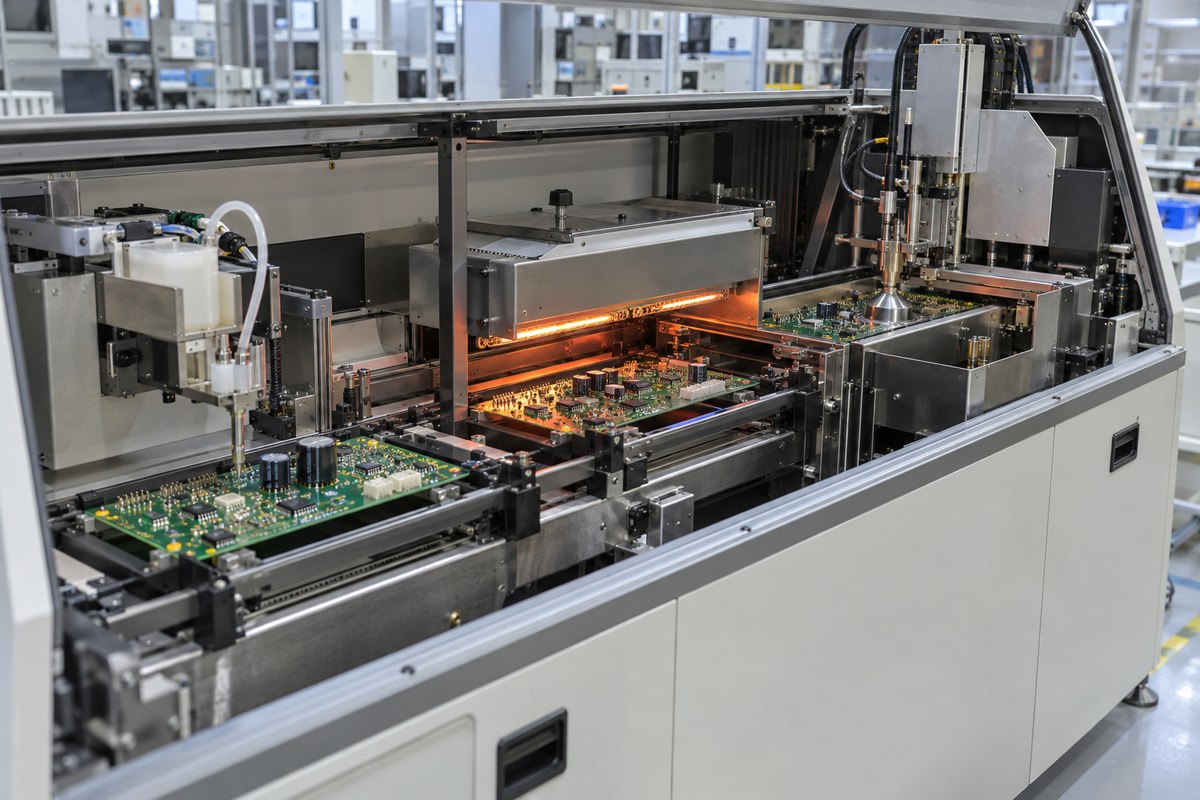
A production cycle normally follows five connected stages:

  1. Flux application: Flux is deposited only where the selected through-hole joints need it.
  2. Preheating: The PCB and component leads are brought to a suitable temperature so that the flux activates and the joint can accept solder.
  3. Localized soldering: A nozzle creates a stable mini-wave and follows the programmed path beneath the required pins.
  4. Cooling: The solder solidifies while the component and PCB remain stable.
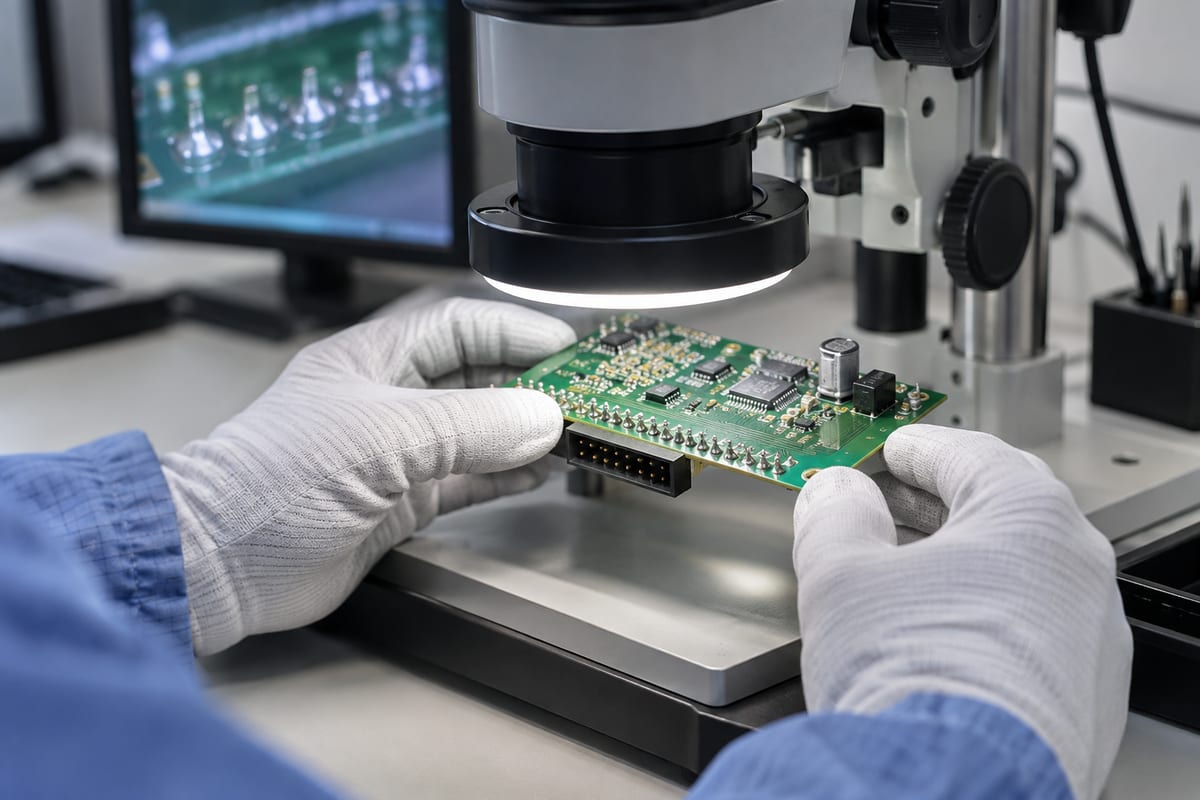
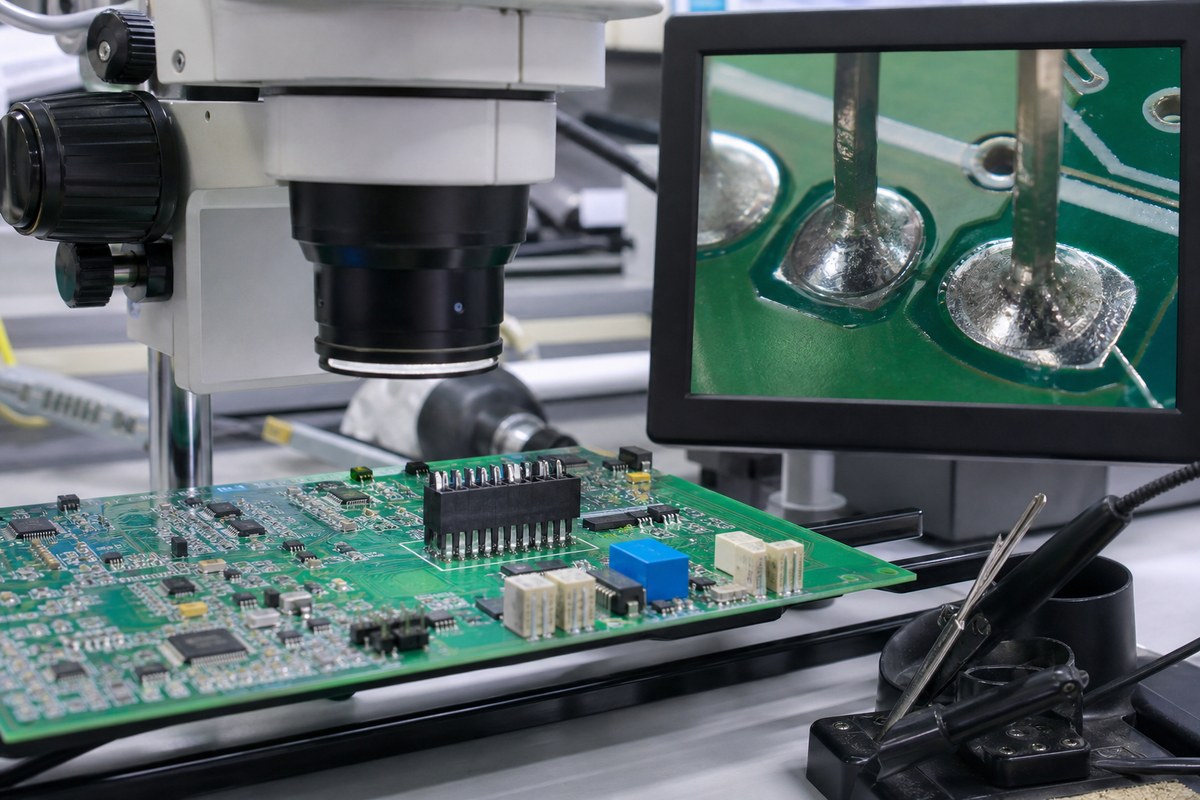
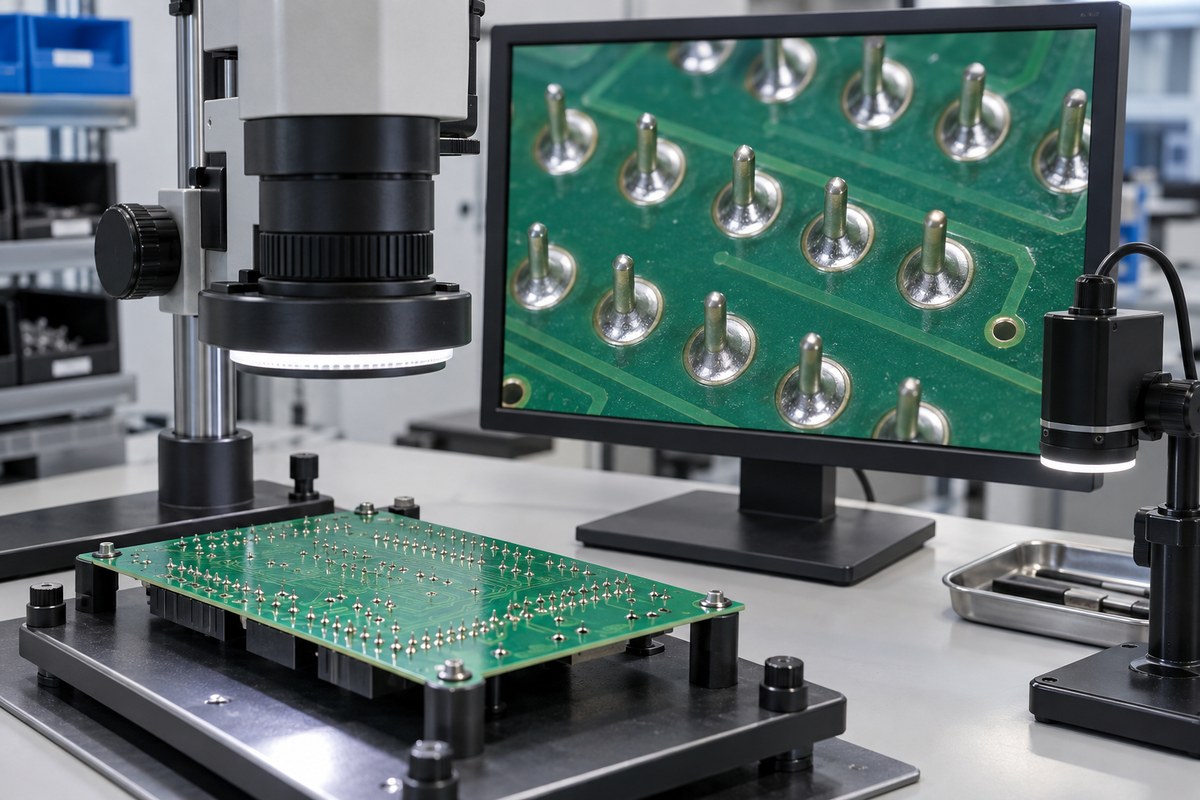
  5. Inspection: The finished joints are checked for wetting, barrel fill, bridging, solder balls, damage, and other agreed acceptance criteria.

These stages cannot be tuned independently. Too much flux may spread beyond the intended area or leave active residue when preheat is insufficient. Weak preheat may force a longer solder-contact time, which can increase copper dissolution and thermal exposure. An unstable solder fountain can make a correct travel path produce inconsistent results.

For this reason, the first article should use the actual PCB, components, alloy, flux, nozzle, and production program. Once the joint results are approved, the program and material combination should remain under revision control.
selective soldering process

How Flux Application and Preheating Prepare the PCB

Flux prepares the metal surfaces for wetting. It removes light oxides from the PCB finish and component leads, then helps molten solder spread into the plated hole. Selective equipment usually applies a controlled drop, jet, or spray pattern around the target area rather than coating the complete underside.

The deposit must reach the joint without flooding nearby components. Too little flux can cause non-wetting or incomplete barrel fill. Too much flux can splash, spread under low-clearance components, create solder balls, or leave residues that have not received enough heat to become benign. Flux chemistry must also match the alloy, board finish, cleaning plan, and product reliability requirements.

Preheat then activates the flux and reduces the temperature difference between the assembly and the molten solder. This is especially important for thick PCBs, heavy-copper constructions, large connector pins, and pins tied to power or ground planes. These structures draw heat away from the barrel. Without enough preheat, solder may wet the bottom pad but fail to rise adequately through the hole.

More heat is not always the answer. Excessive preheat can exhaust the useful flux activity before solder contact, stress temperature-sensitive parts, warp the PCB, or reduce the margin for nearby low-mass joints. A stable profile prepares the most demanding joints without overheating the rest of the assembly.

How the Solder Nozzle Forms Through-Hole Joints

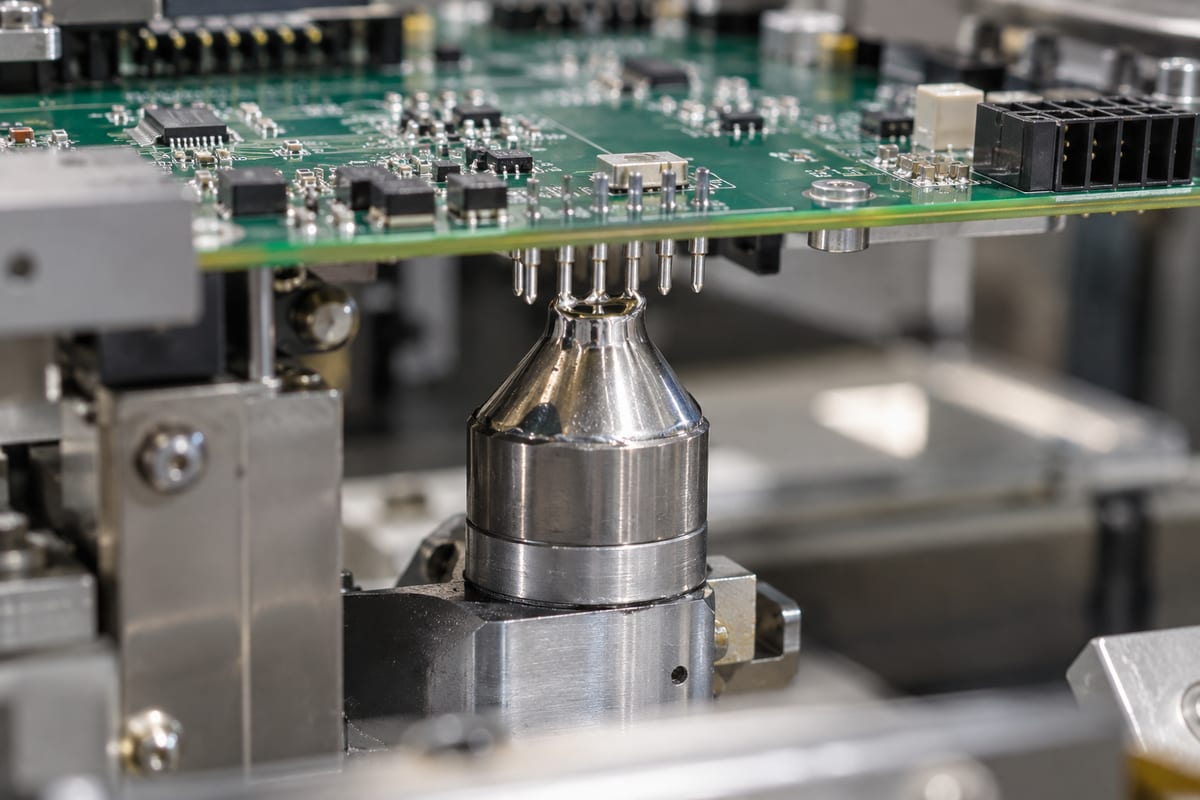
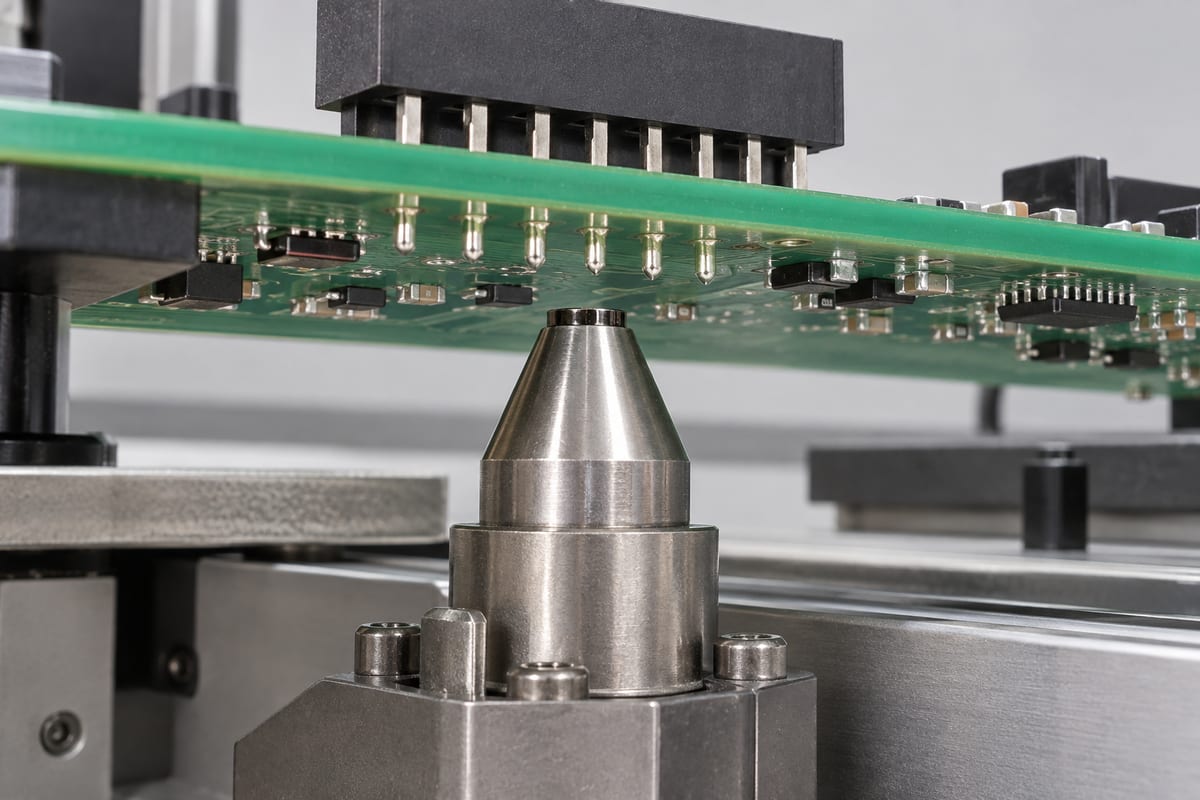
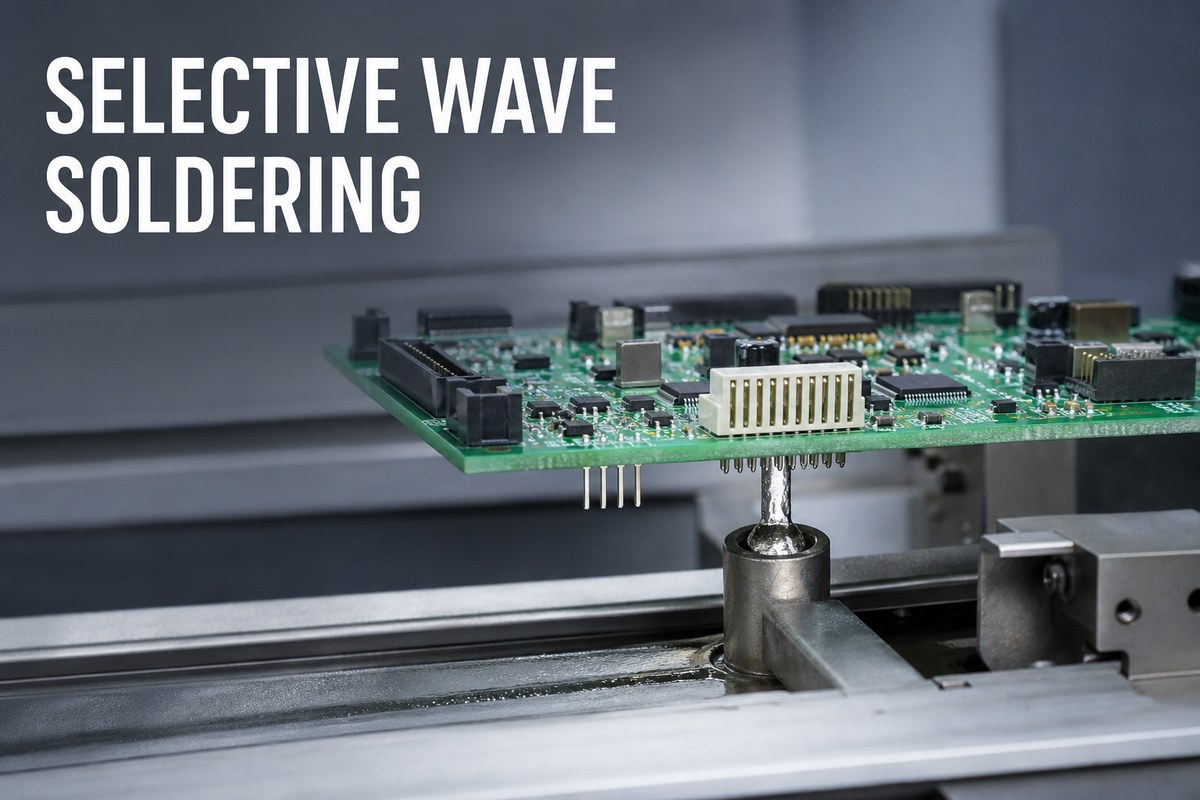
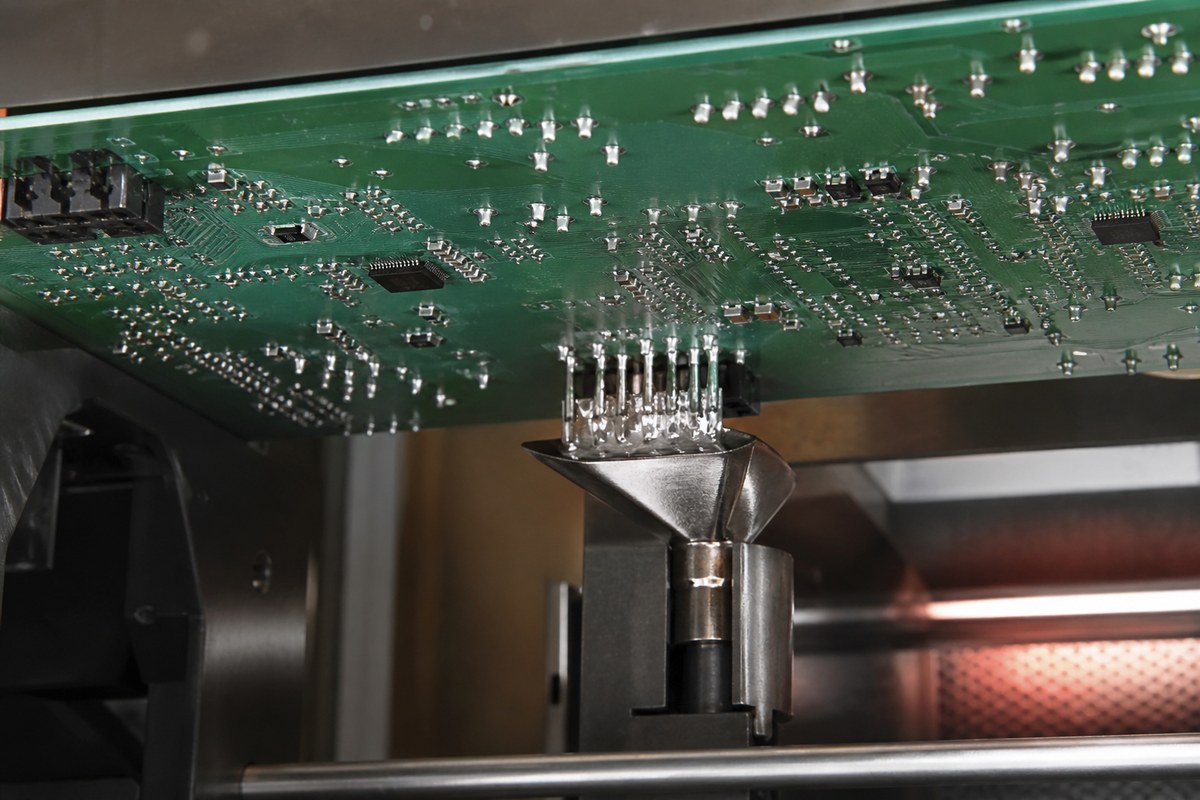
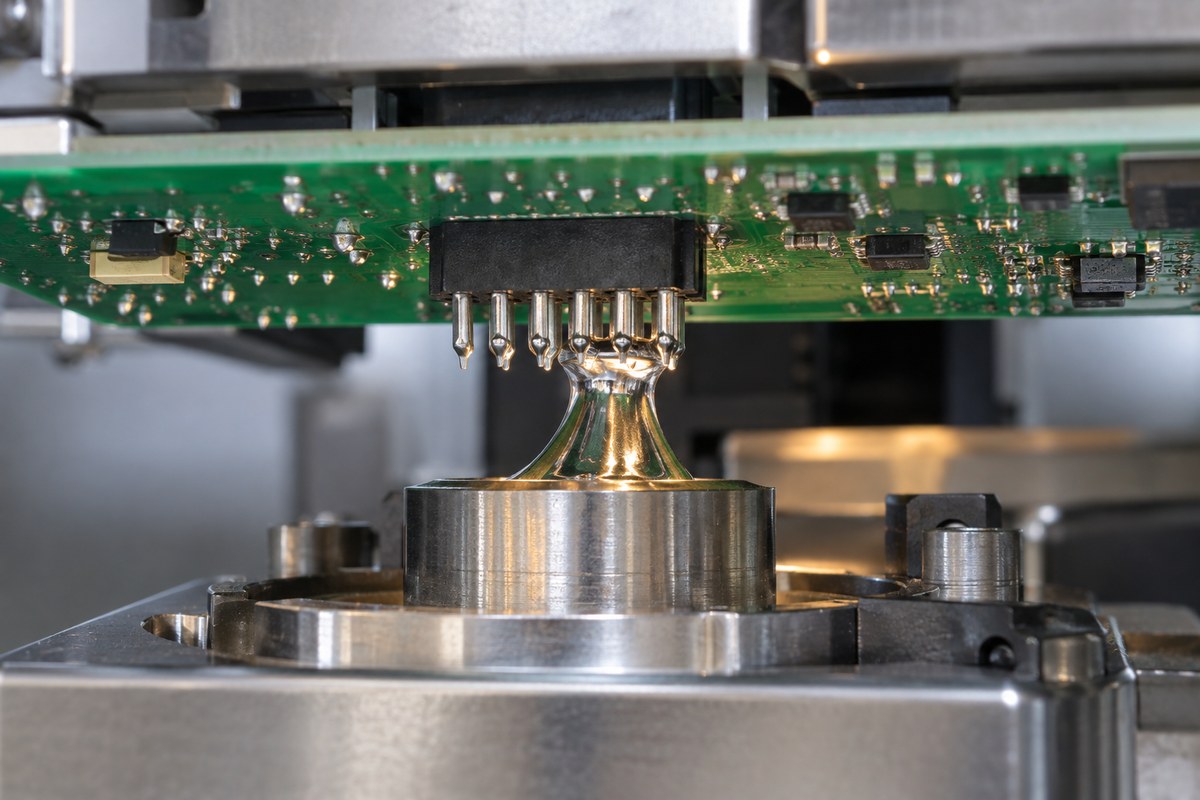
The nozzle pumps molten solder into a small, continuously flowing fountain. The PCB or nozzle moves until the selected pins enter the controlled solder wave. Heat transfers through the leads, pads, and plated barrels; activated flux supports wetting; and capillary action helps solder rise through the hole.
selective soldering process

Nozzle diameter and shape must suit the accessible space and joint group. A larger nozzle can transfer more heat and process a row efficiently, but it requires more clearance. A smaller nozzle can reach isolated pins close to bottom-side SMDs, although its narrower thermal capacity may require a different speed or contact time.

Movement is part of joint formation. Approach direction, immersion depth, travel speed, dwell time, solder-flow height, and withdrawal angle affect how solder enters and leaves the joint. If the nozzle pauses too long, the PCB receives unnecessary heat. If withdrawal is poorly controlled, solder may remain between adjacent pins and create a bridge or icicle.

The nozzle also needs a clean and stable surface. Oxide buildup, contamination, uneven solder flow, or incorrect pump behavior can change the fountain even when the program remains unchanged. Routine nozzle maintenance and process checks therefore protect repeatability as directly as the stored motion program.

Which Parameters Control Selective Soldering Results?

The result comes from the combined thermal, chemical, mechanical, and geometric conditions at each joint. The most influential parameters include:

Control If it is too low or too short If it is too high or too long
Flux deposit Non-wetting or poor fill Residue, splashing, or solder balls
Preheat Inactive flux and cold barrels Flux exhaustion, warpage, or component stress
Solder contact Incomplete wetting or fill Excess heat and copper dissolution risk
Travel speed Insufficient heat transfer Bridging or prolonged exposure
Solder-wave height Unstable contact Flooding or contact with nearby areas

Board construction determines how those settings behave. Finished hole size, lead diameter, copper weight, plane connections, thermal reliefs, PCB thickness, surface finish, and component mass can make two visually similar pins need different thermal treatment.

The correct process window therefore comes from the actual assembly, not a universal temperature or speed copied from another job. When one pin is difficult, the team should identify whether the restriction comes from solderability, flux delivery, hole fit, thermal mass, nozzle access, or motion before changing the complete profile.

Selective Soldering Defects and Their Process Causes

Selective soldering defects are usually the visible result of an earlier process condition. Effective correction starts by tracing the defect back to fluxing, preheat, geometry, solder contact, movement, materials, or handling.
selective soldering process
Defect Likely process causes Practical investigation
Bridging Excess contact, tight pitch, poor withdrawal, unstable flow Check path, speed, nozzle, lead length, and mask geometry
Poor barrel fill Low preheat, high thermal mass, weak wetting, unsuitable hole fit Compare difficult pins with ordinary pins and review the thermal path
Non-wetting Oxidized finish or leads, insufficient flux, contamination Check storage, solderability, flux delivery, and surface condition
Solder balls Excess flux, splashing, moisture, inadequate preheat Review deposit volume, drying, material condition, and nozzle stability
Icicles Slow or unstable withdrawal, excess solder contact Review exit direction, travel speed, wave height, and lead protrusion
Pad or barrel damage Excessive heat or repeated touch-up Review contact time, solder temperature, rework history, and PCB condition

Increasing solder temperature can appear to improve fill, but it can also accelerate copper dissolution, shorten the usable flux window, and increase thermal stress. Likewise, adding more flux may temporarily improve wetting while creating residue or reliability concerns elsewhere.

A useful defect review compares the failed joint with a successful joint on the same assembly. Differences in plane connection, pin mass, hole fit, local clearance, nozzle direction, or flux coverage often reveal the actual cause faster than changing several machine settings at once.

Selective Soldering vs Wave Soldering Process Differences

Both methods solder plated through-hole components with molten solder, but they create very different exposure and production conditions.

Process factor Selective soldering Wave soldering
Solder contact Programmed joints or groups Most of the PCB underside
Typical fit Mixed SMT/THT assemblies THT-heavy, wave-compatible layouts
Main setup Flux pattern, nozzle, path, and local profile Conveyor profile, full wave, pallet or masking
Cycle behavior Time grows with the programmed path Many accessible joints solder at once
Main limitation Nozzle access and local cycle time Broad heat exposure and component protection

Selective soldering is often preferable when bottom-side SMDs sit near a limited number of THT locations, when a connector needs more consistency than repeated hand soldering, or when board variants change the required joint locations. Wave soldering can remain more efficient when the underside is designed for broad solder exposure and many through-hole joints must be processed in one pass.

The choice should reflect the actual board. A selective process may avoid a dedicated wave pallet and reduce touch-up, yet its programmed cycle may be slower. Wave soldering may offer higher throughput, but masking, pallet cost, heat exposure, and rework can change the total production result.

Selective Soldering Process for Mixed SMT and Through-Hole Assemblies

Consider a double-sided SMT assembly that receives a multi-pin connector, a relay, and a plane-connected power terminal after reflow. Bottom-side passives sit close to the connector pins, while the power terminal draws heat into a large copper area.

The connector row may suit a shaped nozzle that solders several pins along one controlled path. Nearby SMDs determine the available nozzle diameter and travel direction. The power terminal may need stronger preheat or a separate dwell condition because its copper connection removes heat faster than the connector pins. The relay body and leads must remain clear of the nozzle approach and withdrawal path.

This assembly should not be validated by looking only at the easiest connector pins. Inspection must include the plane-connected terminal, the connector ends where bridging may occur, and any joint close to a bottom-side package. If those locations meet the agreed criteria without excessive touch-up, the process has demonstrated control across the actual thermal and geometric range of the PCB.

If the nozzle cannot reach a pin, the solution may require a layout adjustment, different PCB assembly fixtures or panel support, another nozzle, approved hand soldering for that location, or a different overall soldering method. Programming cannot recover physical access that the assembled board does not provide.

How EBest Circuit Controls the Selective Soldering Process

For a released PCBA project, EBest Circuit reviews the board data, BOM, assembly drawing, component geometry, panel method, soldering requirements, and inspection criteria before production. This helps identify blocked joints, high-thermal-mass pins, tight connector spacing, special alloy or cleaning requirements, and locations that may need separate process treatment.

PCBA process control focuses on the items that determine repeatability:

  • matching the PCB and assembly revisions to the approved production package;
  • confirming component orientation, insertion, lead condition, and accessibility;
  • setting flux, preheat, nozzle, path, and solder-contact conditions for the actual board;
  • checking ordinary joints and thermally demanding joints during the first article;
  • recording the approved process and controlling later changes;
  • inspecting finished joints against the customer’s specified workmanship criteria;
  • completing agreed electrical testing, traceability, and production records.

The customer remains responsible for the released circuit design, component approval, regulatory requirements, and final product validation. EBest Circuit’s role is to turn the approved PCB and PCBA data into a controlled manufacturing process and to resolve manufacturability questions before they become repeated soldering defects.

For a selective-soldering review, send the Gerber files, drill data, BOM, placement file, assembly drawing, component details, quantities, solder alloy, cleaning requirements, and inspection or testing requirements to sales@bestpcbs.com.

FAQs About the Selective Soldering Process

Is selective soldering used before or after SMT reflow?

It is commonly used after SMT reflow. The SMT components are soldered first, and the remaining through-hole connectors, terminals, relays, or other components are then processed at selected locations.

Is selective soldering the same as selective wave soldering?

Selective wave soldering is the common automated method that uses a localized mini-wave or nozzle. “Selective soldering” is the broader term and can include other localized soldering methods.

Can every through-hole component be selectively soldered?

No. The nozzle needs physical access, suitable clearance, a stable thermal path, and a workable soldering surface. Blocked pins or incompatible component geometry may require a layout change or another approved process.

What usually causes poor hole fill in selective soldering?

Common causes include insufficient preheat, high copper mass, unsuitable hole-to-lead fit, weak solderability, inadequate flux activation, or too little solder-contact time. The cause should be identified before raising temperature or dwell time.

Does selective soldering eliminate manual soldering?

It can greatly reduce manual work on accessible, repeatable joint groups. Very low-volume builds, blocked joints, wires, or exceptional component locations may still require a controlled and approved manual operation.

The best selective soldering process is not the one with the highest temperature or the longest contact time. It is the process that delivers enough flux and heat to every required joint, avoids unnecessary exposure elsewhere, and produces repeatable evidence that the complete assembly meets its approved acceptance criteria. Send your PCB files, BOM, quantities, and requirements to sales@bestpcbs.com for a PCBA manufacturing review.
You may also like

Selective Soldering in PCB Assembly: When It Fits
Thursday, September 17th, 2026

Selective soldering in PCB assembly is a strong option when a mixed-technology board needs repeatable through-hole joints without exposing the entire underside to a solder wave. It is not automatically the best choice for every connector or production volume. The decision depends on joint count, nozzle access, nearby SMDs, thermal demand, cycle time, and the evidence required for production release.

EBest Circuit supports PCB fabrication, component sourcing, SMT, through-hole assembly, and manufacturing review within the agreed PCBA scope. If you want to compare selective soldering with wave or controlled hand soldering for a released board, send the PCB files, BOM, quantities, and acceptance requirements to sales@bestpcbs.com.

selective soldering in pcb assembly
Selective soldering targets chosen through-hole joints on a mixed SMT and THT PCB assembly.

What Is Selective Soldering in PCB Assembly?

Selective soldering applies flux, heat, and solder only to chosen through-hole joints or joint groups. A programmed system moves the board or solder nozzle so that molten solder reaches the required pins while avoiding areas that should not contact a full wave.

The method is especially relevant after SMT reflow. A board may already carry bottom-side resistors, capacitors, ICs, or other temperature-sensitive parts, yet still require connectors, relays, transformers, terminals, or switches to be soldered through the board. Selective soldering targets those remaining THT joints.

The process fits best when localization creates a real manufacturing advantage. Typical reasons include:

  • bottom-side SMDs make full-wave exposure difficult;
  • only selected THT joints remain after reflow;
  • a multi-pin connector needs more repeatability than manual soldering can provide;
  • different product variants use different through-hole locations;
  • masking, pallets, or repeated touch-up would add cost and risk.

The method still needs a workable layout and thermal window. A machine can follow a programmed path, but it cannot compensate for a nozzle blocked by a component body, an inaccessible joint, or a connection to heavy copper that never receives enough heat.

Is Selective Wave Soldering the Same as Selective Soldering?

Selective wave soldering is the most common automated form of selective soldering used for through-hole PCB assembly. It creates a small, controlled wave of molten solder through a nozzle and brings that wave to specific joints.

The two terms are often used interchangeably in PCBA discussions, but they are not perfectly identical. “Selective soldering” is the broader description: solder is applied only where needed. “Selective wave soldering” identifies the localized mini-wave or nozzle method used to do it.

This distinction matters when requesting a quotation. A supplier may consider several routes for a difficult joint:

  • a programmable selective mini-wave;
  • a multi-nozzle or dedicated tooling arrangement;
  • controlled hand soldering for very low quantities;
  • a hybrid process in which accessible joints are automated and exceptional joints follow an approved manual method.

The drawing, quotation, or process agreement should therefore identify the intended manufacturing route when it affects cost, repeatability, inspection, or customer approval. For a closer look at the nozzle-based method, see EBest Circuit’s guide to selective wave soldering.

How Does the Selective Soldering Process Work?

The selective soldering process is a connected thermal and wetting sequence. Each stage influences the next, so a defect should not be blamed on the solder-contact step alone.

  1. Flux application

    Flux is applied to the selected area in a controlled pattern. It helps remove oxides and promotes wetting, but the amount and placement must suit the board, component leads, alloy, and cleaning requirements.

  2. Preheating

    Preheat activates the flux, reduces the temperature difference between the board and molten solder, and prepares high-mass joints to accept heat. A board with heavy copper planes, thick construction, or large connector pins may need a different thermal approach from a light, low-mass assembly.

  3. Localized solder contact

    The programmed nozzle approaches a pin, row, or joint group. Pump condition, nozzle geometry, solder height, travel direction, contact time, and withdrawal all affect solder flow and bridge formation.

  4. Cooling and solidification

    The joint must solidify without movement or unnecessary disturbance. Component stability, lead condition, and downstream handling can affect the result even after the solder leaves the nozzle.

  5. Inspection and release

    The completed joints are evaluated against the agreed workmanship criteria. The review should distinguish ordinary joints from thermally difficult pins because an acceptable connector corner may not prove that a plane-connected power pin has sufficient fill.

There is no universal temperature, dwell time, or travel speed that can be copied safely from another assembly. Surface finish, solder alloy, flux, board thickness, copper distribution, hole-to-lead relationship, component mass, and equipment configuration all change the process window.

selective soldering in pcb assembly
A localized mini-wave nozzle brings molten solder to a selected row of through-hole pins.

Selective Soldering vs Wave Soldering: Which Fits the Board?

The correct choice comes from the board architecture and production economics—not from assuming that the more automated method is always better.

Decision factor Selective soldering Wave soldering
Solder exposure Chosen joints or groups Most or all of the board underside
Typical board fit Mixed SMT/THT assembly with limited THT locations THT-heavy assembly or a board designed for broad wave exposure
Bottom-side SMDs Can avoid many populated areas if access is available May require adhesive, masking, a carrier, or a different layout
Joint quantity Efficient when the programmed path remains reasonable Usually faster when many accessible THT joints need soldering
Main setup Program, nozzle selection, fluxing, and thermal profile Wave profile, conveyor setup, pallet or masking when needed
Main limitation Nozzle access and cycle time Broad heat exposure and protection of non-wave-compatible areas
Changeover Program and tooling may support variants Pallets or masking may change with the assembly

Selective soldering usually deserves serious consideration when reflowed bottom-side components sit near the required THT joints and only part of the assembly needs solder. It may also improve consistency for high-pin-count connectors that would otherwise require extensive hand soldering.

Wave soldering can be the better production route when the underside is designed for the wave, the board contains many THT joints, and conveyor processing provides a shorter cycle with acceptable protection and defect risk.

Controlled hand soldering can still be appropriate for prototypes, very low volumes, or isolated joints that a nozzle cannot reach. Its suitability depends on operator control, thermal demand, inspection, and the cost of variation—not simply on the number of boards.

Compare total production impact rather than one process price. Programming, tooling, masking, cycle time, touch-up, inspection, scrap exposure, and future product variants can change the better answer.

PCB Layout Limits: Nozzle Clearance, Thermal Mass, and Joint Access

A selective-soldering review should begin before the PCB layout is frozen. Once tall parts, bottom-side SMDs, connector bodies, panel rails, and copper planes are fixed, the available process window may already be too narrow.

Nozzle clearance

The nozzle needs physical space to approach the joint without contacting adjacent components or exposing them to unstable solder flow. The required keepout is equipment- and nozzle-specific; one universal clearance value should not be placed in a design rule without supplier confirmation.

Review the complete three-dimensional area around the joint, including connector overhang, component bodies, bottom-side packages, board fixtures, panel rails, and the nozzle’s travel and withdrawal path. A pad that looks accessible in a two-dimensional Gerber view may be blocked in the assembled board.

Thermal mass

Pins connected to ground planes, power planes, heavy copper, large pads, or substantial connector hardware can draw heat away from the joint. If the process is adjusted only for those difficult pins, nearby low-mass joints may receive excessive thermal exposure.

Thermal balance should therefore be considered at layout and validation stages. Plane connections, thermal relief design, finished hole size, lead diameter, board thickness, copper weight, and component mass all influence how quickly solder can rise through the plated barrel.

Joint access and solder flow

The lead, pad, solder mask, and hole must support wetting and drainage. Excessive lead protrusion can disturb the wave or encourage bridging; insufficient protrusion or an unsuitable hole-to-lead relationship may make solder flow and inspection more difficult.

The panel also matters. Rails, breakaway tabs, fixtures, and board support must allow the production system to hold the assembly consistently while keeping the required joints accessible.

Before releasing the design, ask the assembler to review the actual component models, board data, panel method, and intended nozzle. That review can reveal whether a layout change, different tooling, wave soldering, or an approved manual operation is more realistic.

selective soldering in pcb assembly
Nozzle access depends on the three-dimensional clearance around pins, bottom-side SMDs, and board support.

Selective Soldering Defects: Bridging, Poor Barrel Fill, and Non-Wetting

Visible defects are outcomes, not root causes. Corrective action should connect the defect to the board condition, material state, and process stage instead of increasing heat or flux without evidence.

Defect What it may indicate What to investigate
Bridging Adjacent pins remain connected by solder Pin spacing, lead protrusion, solder-mask geometry, nozzle path, solder height, travel direction, dwell, and withdrawal
Poor barrel fill Solder does not rise sufficiently through the plated hole Preheat, thermal mass, hole-to-lead fit, flux penetration, solderability, contact time, and blocked gas escape
Non-wetting Solder does not form a reliable bond to the intended surface Oxidation, storage condition, contaminated finish or lead, weak flux action, inadequate heat, and material compatibility
Icicles or peaks Solder stretches during separation Withdrawal behavior, travel speed, contact time, solder condition, and nozzle stability
Solder balls or splashing Solder separates into unwanted deposits Flux quantity, moisture, preheat, board condition, solder turbulence, and nozzle setup
Heat damage Pad, mask, laminate, or component shows thermal stress Excessive temperature or dwell, repeated repair, poor support, and an overly narrow process window

Bridging on a connector does not always mean “too much solder.” The bridge may result from pin geometry, a poor travel direction, inconsistent board height, or a withdrawal path that pulls solder between adjacent leads.

Likewise, poor barrel fill is not solved reliably by extending contact time alone. A plane-connected pin may need more effective preheat, while another pin in the same connector could already be near its thermal limit. The process must satisfy both without creating a new failure.

Inspection should also consider residue, disturbed components, mask condition, pad damage, and evidence of repeated touch-up. If a joint repeatedly needs repair, the underlying layout or process window deserves review.

How to Validate Selective Soldering Before Production

Production validation should prove the process on the actual assembly, using the intended materials, program, tooling, and acceptance criteria. A machine demonstration on a different board does not establish that the released product is ready.

Start by defining what must be proven. The validation set should include the most difficult joints, not only the easiest connector row. Typical challenge points are plane-connected pins, large terminals, shielded areas, tight-pitch connectors, joints near bottom-side SMDs, and locations at the edge of nozzle access.

A practical validation sequence is:

  1. Confirm the PCB revision, BOM, component details, assembly drawing, panel arrangement, solder alloy, flux, and any cleaning restrictions.
  2. Review nozzle access and select the intended automated, wave, hand, or hybrid route for each THT location.
  3. Establish flux, preheat, solder-contact, travel, and withdrawal settings on production-intent equipment.
  4. Run a first article using representative boards and components.
  5. Inspect both normal and high-risk joints against the agreed criteria, including bridging, wetting, barrel fill, residue, and heat damage where applicable.
  6. Record the approved program, tooling, material set, inspection result, and any permitted touch-up method.
  7. Revalidate when a design, component, finish, alloy, flux, panel, tooling, or other controlled input changes enough to affect the process window.

Validation evidence should match the customer’s risk and contractual requirements. It may include first-article inspection records, visual results, process records, photographs, electrical testing, or additional analysis when specifically required. One document should not be treated as proof of every requirement: a process record confirms settings, while inspection or testing confirms the agreed output.

EBest Circuit can review assembly access and coordinate PCB fabrication, sourcing, SMT, through-hole processing, and agreed inspection or testing as part of its PCB assembly service. The released files and quotation should define the exact production and acceptance scope.

selective soldering in pcb assembly
Inspection of representative and thermally difficult through-hole joints supports production validation.

FAQs About Selective Soldering in PCB Assembly

1. When is selective soldering a good choice for a PCB assembly?

It is a good candidate when a mixed SMT/THT board has a limited number of through-hole joints, bottom-side components should avoid full-wave exposure, and the target joints have adequate nozzle access and a stable thermal window.

2. Can selective soldering replace wave soldering on every board?

No. A THT-heavy board may be faster and more economical to wave solder. Selective soldering can also be unsuitable when components, fixtures, or panel features block the nozzle, or when the programmed cycle becomes too long.

3. Is selective soldering always better than hand soldering?

No. It can improve repeatability and reduce operator variation for suitable joints, but controlled hand soldering may remain practical for prototypes, very low volumes, or exceptional joints that cannot be reached automatically.

4. What information is needed to assess selective-soldering feasibility?

Provide the released PCB data, drill and fabrication information, BOM with component details, placement and assembly drawings, panel requirements, order quantity, solder and cleaning restrictions, and the required workmanship, inspection, test, and traceability criteria.

5. What most often prevents a board from using selective soldering?

Common blockers include insufficient nozzle clearance, inaccessible joints, excessive thermal imbalance, unsuitable lead or hole geometry, obstructive panel tooling, and a production volume or joint count that makes another process more efficient.

Need a manufacturing review for selective soldering in PCB assembly? Send your released data, expected quantities, difficult THT locations, and acceptance requirements to sales@bestpcbs.com so EBest Circuit can compare the available PCBA routes for your project.

You may also like

Selective Wave Soldering: Avoid Mixed-Assembly Rework
Monday, August 10th, 2026

Selective wave soldering targets programmed through-hole joints instead of exposing the full board underside. It can protect reflowed components and improve consistency, but only when the layout, nozzle access, production volume, and acceptance criteria support the process.

selective wave soldering
Selective wave soldering for targeted through-hole joints on a mixed-technology PCB assembly.

What Is Selective Wave Soldering?

Selective wave soldering is an automated process that applies flux, heat, and molten solder to chosen plated through-hole joints. A small nozzle or mini-wave reaches the target area without deliberately exposing the full board underside.

It is often used after SMT reflow to solder connectors, relays, transformers, terminals, and switches. Compared with extensive hand soldering or full-wave exposure, it can reduce masking, operator variation, and touch-up.

The process still needs enough nozzle clearance, flux coverage, and heat transfer. The real question is whether the released assembly provides a stable and inspectable process window.

When Does Selective Wave Soldering Prevent Rework?

Selective wave soldering is most useful when a board has reflowed SMDs on the bottom side but only a limited number of through-hole joints.

It may reduce rework when:

  • Bottom-side SMDs are close to through-hole joints.
  • Heat-sensitive parts should avoid a full solder wave.
  • High-pin-count connectors need repeatable soldering.
  • Hand soldering would add too much variation.
  • Product variants require different through-hole locations.

It is not always the lowest-cost choice. Full wave soldering may suit a through-hole-heavy board, while controlled hand soldering may suit a simple prototype. Early supplier review helps identify access or layout problems before production.

Selective Soldering vs Wave Soldering

Both processes create through-hole joints, but they expose the PCB differently. The best choice depends on layout, volume, setup cost, cycle time, and rework risk.

FactorSelective solderingWave soldering
ContactTargeted jointsFull underside
Best fitMixed SMT/THTTHT-heavy boards
SetupProgram and nozzleProfile and pallet
SpeedSlower pathFaster for many joints
Main riskAccess and cycle timeHeat, masking, rework

Compare total cost, not only unit price. Include programming, pallets, first-article inspection, manual touch-up, and scrap risk. A selective process may cost more per cycle but less overall if it prevents masking and rework.

How Does the Selective Wave Soldering Process Work?

The selective wave soldering process normally includes five stages:

  • Flux: A controlled amount reaches the selected joints.
  • Preheat: Heat activates the flux and reduces thermal shock.
  • Soldering: A programmed nozzle contacts each joint or joint group.
  • Cooling: Joints solidify without disturbance.
  • Inspection: Results are checked against the approved criteria.

Board thickness, copper distribution, surface finish, hole fit, alloy, flux, and component mass all affect the process window. A generic temperature or dwell time cannot fit every PCB.

A first article should prove that the selected settings work on the actual assembly. Approved programs, materials, and inspection criteria should then remain under revision control.

selective wave soldering
A localized solder nozzle targets a selected through-hole connector area.

Selective Wave Soldering Design Rules

Selective wave soldering design rules should protect nozzle access and support consistent heat transfer.

Review before PCB release:

  • Nozzle access: Nearby parts must not block the target joint.
  • Clearance: Keep enough space from SMDs, shields, and tall bodies.
  • Lead protrusion: Allow solder contact without creating shorting risk.
  • Hole fit: Support component insertion and solder flow.
  • Pad and mask: Promote wetting without encouraging bridges.
  • Thermal balance: Review joints connected to planes or heavy copper.
  • Panel access: Rails and tooling must not block the path.
  • Inspection access: Finished joints must be assessable.

Missing these checks can lead to blocked nozzles, connector bridging, or poor fill on high-mass pins. The result may be manual rework, new tooling, or a PCB revision.

EBest Circuit (Best Technology) can review manufacturability and assembly access within the agreed production scope. The customer remains responsible for component approval, circuit function, safety spacing, and the released design.

How Do You Prevent Selective Soldering Defects?

Selective soldering defects should be traced to the actual board condition and process variable. Increasing heat without finding the cause may fix one joint and damage another.

DefectCommon causeCheck
BridgingTight spacing or excess solderMask, path, withdrawal
Poor barrel fillLow heat or high thermal massPreheat, dwell, hole fit
Non-wettingOxidation or weak flux actionStorage, finish, flux
IciclesPoor withdrawal or excess contactPath, dwell, nozzle
Solder ballsExcess flux or splashingFlux, preheat, setup
Pad damageExcess heat or repeated repairProfile and repair history

A practical validation plan includes:

  • Confirm the BOM, PCB revision, drawing, and program.
  • Run a first article with production materials and equipment.
  • Inspect ordinary and high-thermal-mass joints.
  • Agree on barrel fill, bridging, residue, and damage criteria.
  • Record approved settings and permitted touch-up.
  • Revalidate after significant material or design changes.

Inspection must follow the customer’s specified workmanship and contractual requirements. The assembler should provide evidence for the agreed PCBA scope, while the customer owns final product acceptance.

selective wave soldering
Inspection helps verify solder-joint quality against the agreed acceptance criteria.

What Should a Selective Wave Soldering RFQ Include?

An incomplete RFQ can hide access conflicts, difficult connectors, and special inspection needs. These discoveries often lead to quotation changes later.

Send the following files and requirements:

  • Gerbers, drill data, and fabrication drawing.
  • BOM with approved manufacturer part numbers.
  • Placement data and assembly drawings.
  • Panel requirements and relevant component datasheets.
  • Order quantity, repeat demand, and product variants.
  • Solder alloy, cleaning, and material restrictions.
  • Workmanship, hole-fill, and inspection requirements.
  • Test, traceability, and packaging instructions.

Also identify areas where touch-up is prohibited or downstream coating creates a special constraint. A complete package helps the supplier compare selective soldering, wave soldering, hand soldering, or a hybrid route on the same released scope.

A Mixed-Technology PCB Assembly Example

Consider a double-sided SMT assembly with a multi-pin connector, power terminal, and relay added after reflow. Bottom-side passives sit near the connector, while the terminal connects to a large copper area.

Full wave soldering may require a pallet to protect the SMDs. Hand soldering may add variation and labor. A selective-soldering review would instead check:

  • Nozzle access around the connector pins.
  • Extra heat demand at the power terminal.
  • Relay clearance and lead protrusion.
  • First-article results at both normal and difficult joints.

If the process window is stable, selective soldering may reduce masking and touch-up. If the nozzle cannot reach the connector, the layout, tooling, or soldering method should change before production.

This is a manufacturing example, not a claim about a specific customer project. The final decision depends on the actual PCB, BOM, volume, and acceptance requirements.

How Can EBest Support Selective Wave Soldering?

EBest Circuit (Best Technology) supports customers within the PCB and PCBA manufacturing scope. Support may include:

  • PCB manufacturability and assembly-access review.
  • PCB fabrication and revision control.
  • BOM review and sourcing coordination.
  • SMT and agreed through-hole assembly.
  • Selective-soldering feasibility review.
  • First-article inspection and agreed testing.
  • Required traceability and production records.

The customer retains responsibility for circuit design, component approval, firmware, regulatory requirements, certification, and final product validation. Responsibilities should be defined by the quotation, released files, and approved inspection or test requirements.

Selective Wave Soldering FAQs

Is selective wave soldering the same as selective soldering?
It is a common selective-soldering method that uses a localized solder wave or nozzle. Because “selective soldering” can also describe other localized methods, the RFQ should name the intended process.

Can selective soldering replace wave soldering on every PCB?
No. Nozzle access, joint count, cycle time, thermal mass, volume, and cost may make wave soldering or another process more suitable.

Does selective wave soldering eliminate hand soldering?
It can reduce manual work when joints are accessible and the program is stable. Blocked or very low-quantity joints may still require an approved alternative.

What causes insufficient hole fill during selective soldering?
Common causes include inadequate heat, high copper mass, poor hole fit, weak solderability, flux problems, or an unstable nozzle path.

What files are needed for a selective-soldering quotation?
Provide PCB fabrication data, BOM, assembly files, component details, quantities, panel information, inspection criteria, and test or traceability requirements.

Need help deciding whether selective wave soldering fits your mixed-technology PCBA? Send your released PCB files, BOM, quantities, and acceptance requirements to sales@bestpcbs.com for a manufacturing review and quotation.

You may also like