PCB manufacturing PCB manufacturing
Home > Blog

through-hole assembly

How Is Component Lead Forming Done Before PCB Assembly?
Friday, October 23rd, 2026

Component lead forming bends and trims a component's terminals to fit the PCB footprint without transferring damaging loads into the package. A usable form has more than the right spacing: it also needs the correct bend location, radius, body clearance and lead length. For through-hole assemblies, we need the exact component part number and assembly drawing to resolve those dimensions before insertion, rather than forcing a mismatched component into the board.
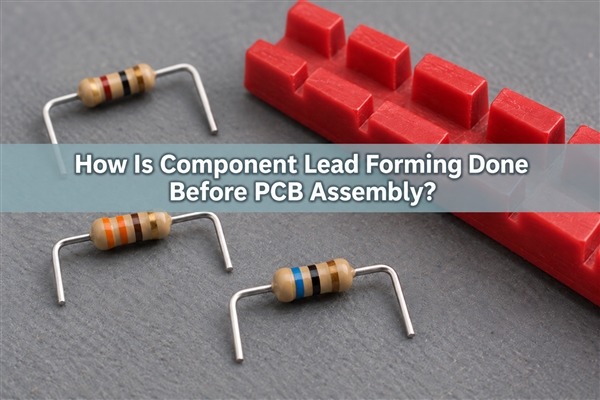
Component lead forming with preformed axial resistors and a forming jig; AI illustration

What Is Component Lead Forming?

Electronic component lead forming is the controlled preparation of lead geometry before assembly. It can produce a simple right-angle bend, a specified offset or an approved stand-off shape. Trimming controls lead length; forming controls the path and position of the lead. They are related operations, but one does not automatically establish the requirements for the other.

The component body is not a handle for bending its leads. A part may still fit the holes after rough handling while its lead-to-body interface has been damaged. Fit, package condition and electrical performance therefore answer different acceptance questions. An acceptable shape also has to survive handling between the forming station and PCB insertion.

Which Dimensions Should a Lead Forming Drawing Specify?

The drawing should define the finished shape using identifiable reference points, not just a distance dialed into a tool. Include the component outline, lead cross-section and tolerances alongside the PCB footprint. A center-to-center pitch and an outside-to-outside measurement are not interchangeable.

Drawing input What needs to be defined What it prevents
Component identity Manufacturer, exact part number, package and drawing revision Applying another package's forming limits
Lead size Round-wire diameter or rectangular-lead width and thickness Selecting a die or hole for the wrong cross-section
Body-to-bend clearance The body reference and the start of the permitted bend Bending into a seal, coating or molded exit
Bend geometry Inside radius, angle, direction and any approved offset A sharp crease or an uncontrolled twist
Finished lead pitch Center-to-center spacing, measurement height and tolerance Accepting a tool setting instead of the released part
Body position Orientation, polarity and required stand-off Reversed parts or contact with nearby features
Trimmed length Lead-tip position relative to the board and soldering requirement Insufficient protrusion or interference below the PCB

For a multi-lead package, one total span is insufficient: individual terminal positions must match the footprint. When a supplier changes the package outline or lead dimensions, the previous forming setup needs review even if the electrical description is unchanged.

How Do You Choose the Lead Bend Radius?

Choose the bend radius from the exact component's approved forming instructions. Lead diameter alone is not enough when package construction, lead material, plating and bend direction differ. A radius measured at the inside of the curve must not be confused with the centerline radius.

For example, onsemi's axial plastic-package guidance AND8390/D specifies a radius no smaller than the lead diameter, limits the angle to 90 degrees and calls for a single forming operation. Its body-to-bend minimum is 1.5 times the typical lead diameter, with at least twice the diameter preferred. These are conditions for the packages covered by that guidance, not a universal rule for resistors, LEDs, capacitors or all transistor packages.

The drawing must also leave enough straight lead for the support tool. If the required footprint forces the bend into a prohibited region, changing the footprint or using an approved preformed component is preferable to tightening the bend until the part fits. Do not resolve a clearance conflict by silently replacing the manufacturer's radius requirement.

How Can You Prevent Stress at the Component Body?

Support the lead between the package and the forming point so that the tool takes the reaction load. Pulling the free end while holding the body allows that load to reach the lead exit. The support must restrain the lead without cutting it, stripping the finish or crushing the package.
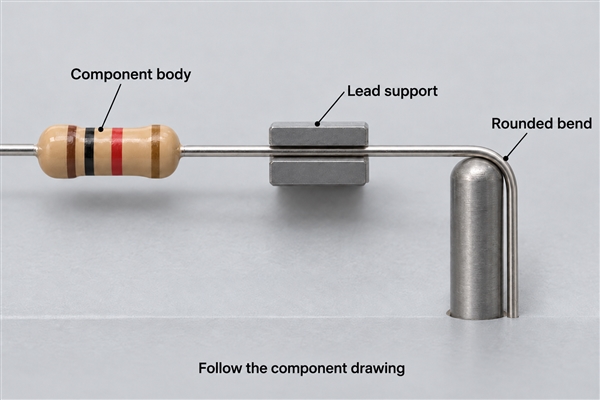
Lead support between the component body and rounded bend, shown as an illustrative setup

Glass packages require particular care. For the Vishay SOD-57, SOD-64, DO-35 and DO-41 glass diodes covered by document 86158, the body-to-bending-position distance is greater than 1.5 mm. The specified fixture grips the lead wires and keeps mechanical load off the glass body. This is a package-specific requirement, not permission to grip the glass itself.

That document includes a minimum clamping-force instruction expressed as 2.5 kg. It must be interpreted with the original fixture arrangement and applicable device documentation; it is not a general hand-pliers setting. A controlled setup must distinguish sufficient restraint from excessive lead deformation. Unexpected tool marks or package movement require a setup review, not simply more force.

How Do Axial and Radial Lead Forming Differ?

Axial component lead forming positions leads that leave opposite ends of the body. The finished geometry must accommodate the body length, clearances on both sides and the two bends. An axial component lead former therefore needs space for the actual body and suitable support for both wires, not merely a groove labeled with the target pitch.

Radial lead forming deals with leads leaving the same side of the body. Changing their spacing can load the nearby lead exits, especially when the available straight length is short. Radial component lead forming also needs to preserve polarity, lead order and the component's intended seating height. Do not treat every two-lead radial part as mechanically equivalent to an axial resistor.

Flat transistor leads introduce another issue: bending through the thin dimension is mechanically different from sideways bending across the width. A TO-92 lead forming tool must match the particular pin arrangement and approved bend location. The package name alone does not establish a permitted offset or bending direction.

How Do You Select a Component Lead Forming Tool?

Select a component lead forming tool by lead shape, supported diameter or thickness, bend profile and finished spacing. An electronic component lead former should hold the part consistently without using its body as a reaction stop. Accessibility matters too: the tool must leave room for the required straight section near the package.

Tool approach Useful role Check before use
Fixed or adjustable lead bending and component forming tool Repeatable simple axial bends Groove geometry, body clearance and released pitch
Component lead forming pliers Local offsets or specified lead shapes Jaw profile, contact marks and operator repeatability
Component lead forming machine Repeated parts with controlled feed and setup Package compatibility, tooling condition and first-piece results

A component lead forming kit can help with prototype work, but its available shapes do not override component requirements. The same applies to a lead forming tool for resistors and capacitors: sharing a tool is reasonable only where the two devices' permitted geometry and support conditions actually match.

For larger runs, an electronic component lead forming machine needs a verified setup rather than a copied setting from a different package. A component lead former with multiple stations should maintain the same reference orientation through feeding, forming and cutting. Before releasing a batch, compare the first formed parts with the approved drawing and check that feeding has not reversed the component orientation.

How Should Component Leads Be Trimmed?

Trim to the specified finished length while preventing the cutting action from pulling on the lead-to-body interface. Support and cutting sequence depend on the package and tooling. Keep cut fragments away from parts and PCB assemblies, and inspect the cut end for a burr that could obstruct insertion.

For the glass-diode packages in Vishay document 86158, simultaneous cutting of both leads is not permitted in the illustrated arrangement. Separate cutting steps or a staggered cutting arrangement are shown instead. The document allows simultaneous bending with its specified support conditions. Cutting and bending are therefore not interchangeable when deciding which operations can be performed together.

Where trimming occurs after insertion, support must also protect the board, pads and any existing solder connection. For a through-hole component fitted to a multilayer PCB, use the finished board thickness and seating height to establish the required lead length, not the layer count. The finished protrusion should come from the applicable assembly requirement, not an arbitrary universal length. A shorter lead is not automatically a better assembly if it compromises soldering or inspection access.

How Do You Check Lead Pitch After Forming?

Check pitch after removing the forming load, at the drawing's specified measurement location. Elastic recovery can make the released part differ from the tool's nominal setting. A measurement made while the part is still constrained can hide that difference.
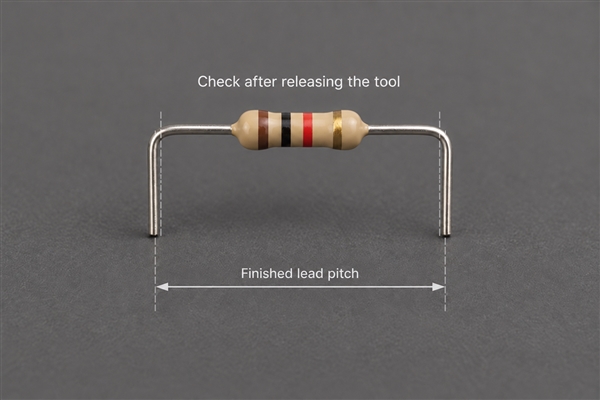
Released axial component with center-to-center finished lead pitch indicated; illustrative geometry

For two equal round leads measured across their outside surfaces, subtract one lead diameter to obtain the center-to-center distance. As a dimensional example, a 10.60 mm outside span with two 0.60 mm leads gives a 10.00 mm center pitch. This calculation assumes parallel leads of equal diameter at that measurement height; it is not a forming tolerance recommendation.

Check lead parallelism and seating height as well as pitch. For our FR4 PCB manufacturing, the drawing's finished-hole size and position must be considered with the actual lead envelope. A nominal drill diameter is not the finished plated-hole diameter. Do not spread or squeeze the component against the board to conceal a mismatch.

What Should You Inspect After Lead Forming?

Inspect the component body, lead exits, bends, finish and final dimensions before accepting the formed parts. Compare with the incoming condition where a mark or crack may already have existed. Appearance alone cannot establish whether a hidden connection or seal remains intact.
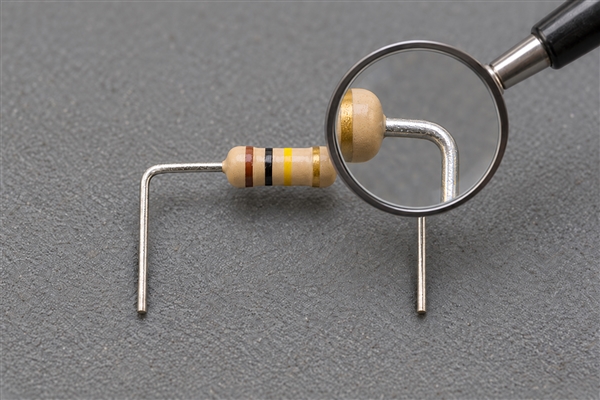
Illustrative magnified inspection of a formed lead and component body
Inspection area Look for Follow-up when it does not match the requirement
Body and lead exit Cracks, chipped coating, displacement or a changed lead exit Segregate the part and assess package damage
Bend Creasing, twisting, inconsistent radius or repeated rework Check the profile and support arrangement
Lead surface Deep jaw marks, exposed base metal or damaged finish Compare with the device's permitted tooling marks
Dimensions Pitch, parallelism, angle, length and stand-off Measure in the released state against the drawing
Insertion fit Leads aligned with holes without forced reshaping Review both formed geometry and PCB footprint
Electrical condition Results required by the device and test plan Record failures without treating continuity alone as full qualification

An inspection record is most useful when it identifies the part number, lot, drawing revision, setup, sampled quantity and measured dimensions. A photograph can document a visible condition, but cannot prove a numerical radius or hidden seal integrity by itself. Abnormal parts need disposition before insertion, when access to the lead exits is still clear.

How Can You Keep Lead Forming Consistent Across a Batch?

Use an approved first piece, defined setup controls and checks at meaningful change points. Tool wear, a new component lot or a changed package can alter the output even when the operator uses the same setting. Record the released dimensions rather than treating a machine setting as the acceptance result.

Separate unformed, accepted and held parts so rejected pieces cannot re-enter production. Packaging between operations should protect the formed leads from being compressed or tangled. If a component needs repeated straightening to pass the insertion check, stop and resolve the mismatch rather than cycling the lead through additional bends.

For a new footprint, our PCB prototype manufacturing can provide the actual board for a fit review before the design moves to volume assembly. The useful result is a checked component-and-board combination, not a nominal pitch verified on only one side of that interface.

What Information Do We Need for Through-Hole Assembly?

We need the BOM with exact manufacturer part numbers, PCB fabrication data, assembly drawing, orientation requirements and any approved lead-form dimensions. Include the original component instructions when a bend, stand-off or trimming sequence is critical. State whether parts arrive unformed, factory-preformed or customer-prepared.

At EBest Circuit (Best Technology), our PCB assembly service includes through-hole and mixed assembly, incoming inspection, DFA review, insertion and wave soldering. We support tube, tray and loose-part supply as well as other listed packaging formats. The suitable preparation route depends on the component and build requirements; we do not apply one bend specification to every package.

For component lead forming services within a PCBA project, send the drawing, quantity and required inspection records to sales@bestpcbs.com. We can review those inputs with your assembly requirements before quotation. If the package instructions and footprint conflict, that conflict needs an agreed resolution before production.

Component Lead Forming FAQs

How to Clean and Form Component Leads Before Soldering?

Check incoming finish condition before forming. Use only a cleaning method compatible with the component, plating and approved process; abrasive removal of finish or an unapproved chemical treatment can create a solderability problem. Suspect corrosion requires assessment rather than polishing the part until it looks clean. Confirm acceptable surface condition before releasing the part for forming and soldering.

When Shall Sleeving Be Placed on a Component Lead Before Forming?

Where the approved assembly requires insulation sleeving and the finished bend would prevent it from sliding into place, fit the sleeve before that bend. Confirm its final position, temperature suitability and clearance from the solder joint. Do not assume every formed lead needs sleeving or trap a sleeve in a tooling contact area.

Can Through-Hole Forming Rules Be Used for SMT Leads?

Not automatically. SMT component lead forming also involves seating-plane and coplanarity requirements, plus the specific package's permitted reshaping method. A through-hole bend or spacing instruction does not establish an acceptable gull-wing lead profile. Use the component's approved surface-mount geometry rather than adapting the axial-wire examples without verification.

Can a 3D-Printed Lead Forming Jig Replace Metal Tooling?

A resistor lead forming tool made by 3D printing may be useful for a checked prototype geometry. It still needs adequate stiffness, smooth contact surfaces and appropriate ESD controls for the parts being handled. Wear or deflection can change the finished dimensions. It should not be treated as a qualified production fixture merely because one component fits.
You may also like

Single Sided PCB Assembly for Cost-Efficient Production
Friday, October 2nd, 2026

Single sided PCB assembly can reduce production complexity when every component fits on one assembly side and the soldering process remains straightforward. The real advantage is not simply having fewer populated surfaces. It is avoiding unnecessary second-side placement, extra board handling, and additional process steps while still meeting the product’s electrical, mechanical, thermal, and inspection requirements.

EBest Circuit manufactures bare PCBs and assembles customer-designed boards with SMT, through-hole, or mixed component populations. By reviewing the approved PCB data, BOM, component packages, polarity information, and test requirements together, we help customers move from prototype quantities to repeat production with fewer avoidable process changes. For a quotation or DFM review, contact sales@bestpcbs.com.

single sided PCB assembly
A single-sided PCBA keeps all component bodies accessible on one populated surface.

What Is Single Sided PCB Assembly?

Single sided PCB assembly means that all mounted components are placed on one side of the finished circuit board. This describes the component population, not necessarily the number of copper layers inside the PCB. A board can have one copper layer and components on one side, but a multilayer PCB can also use single-sided assembly when all packages are mounted on the same surface.

That distinction matters because “single sided” can refer to three different features:

  • A single sided PCB has one conductive copper layer.
  • Single sided assembly places all components on one side of the board.
  • Single-pass soldering describes a production route, but it does not automatically define the board’s copper-layer count or component layout.

Traditional single-layer boards often combine through-hole parts inserted from the component side with leads soldered on the copper side. An SMT design usually places both pads and components on the copper-patterned surface. Mixed technology can combine SMT and through-hole parts on one populated side, although the solder joints may be formed through different processes.

The practical benefit appears when the circuit is simple enough to remain accessible on one side. Fewer placement surfaces can simplify tooling, handling, visual inspection, repair, and process control. Once jumpers, awkward package orientations, thermal crowding, or excessive board area are needed to preserve that restriction, the single-sided format may no longer be the lower-cost solution.

How Are SMT and Through-Hole Components Placed on a Single Sided PCB?

SMT and through-hole components can share a single sided PCB, but their mounting and soldering paths are different. Surface-mount packages sit directly on pads. Through-hole parts pass through drilled holes, and their leads are soldered on the opposite surface. The placement plan must therefore consider component access, lead direction, solder contact, and the order of each operation.

For SMT-only assembly: solder paste is printed onto the pads, components are placed on the same surface, and the board passes through reflow. This is efficient for compact resistors, capacitors, ICs, and other packages that are suitable for automated placement.

For through-hole assembly: parts are inserted from the component side and soldered from the reverse side by wave soldering, selective soldering, or a controlled manual process. Connectors, transformers, relays, and mechanically loaded parts often use this method when their package or retention requirements make through-hole mounting appropriate.

For mixed assembly: SMT parts are usually placed and reflowed first. Through-hole parts are then inserted and soldered using a process compatible with the component bodies, spacing, and exposed SMT features. Pallets or selective soldering may be required when previously mounted parts must be protected from the solder wave.

Keeping all components on one side can make markings easier to read and service access more direct. However, the layout still needs adequate spacing around connectors, tall parts, polarized packages, test points, and soldering areas. A one-sided population only creates value if those features can be assembled without excessive manual correction or special handling.

How Does Single Sided PCB Assembly Move Through Production?

Single sided PCB assembly moves through production by matching the released board data and BOM to a controlled SMT, through-hole, or mixed-assembly route. A typical build follows this sequence:

single sided PCB assembly
A controlled process route can combine SMT and through-hole components on one assembly side.
  1. Data and BOM review: Gerber or ODB++ data, drill files, drawings, centroid data, BOM details, component orientations, and revision identifiers are checked for agreement.
  2. Bare-board fabrication and inspection: the PCB is built to the approved stackup, copper, solder-mask, surface-finish, outline, and hole requirements before assembly begins.
  3. Material preparation: component identity, package, value, quantity, moisture sensitivity, polarity, and approved substitutions are controlled against the released BOM.
  4. SMT processing where required: solder paste is printed, paste deposition is checked, components are placed, and the board is reflowed under an established thermal profile.
  5. Through-hole processing where required: leads are inserted, formed when permitted, and soldered by the selected wave, selective, or manual method.
  6. Cleaning, inspection, and testing: residues are managed according to the process specification, solder joints and component placement are inspected, and the agreed electrical tests are completed.

This route may be shorter than a two-sided assembly because the board does not require a second stencil print and placement cycle. It may also avoid the support, adhesive, or reflow considerations created by components on the underside. The actual saving depends on the component mix: a board dominated by manual through-hole work can still require substantial labor even though every part is on one side.

Stable repeat production depends on preserving the approved footprint geometry, solder volumes, component orientations, and process sequence. When a prototype uses hand-soldered substitutions or temporary jumpers, those exceptions should be resolved before the same board is treated as a production-ready single-sided assembly.

What Determines Single Sided PCB Assembly Cost?

Single sided PCB assembly cost is determined by the complete production route, not by component-side count alone. A one-sided population often costs less when it removes a second placement cycle, reduces fixtures and handling, and supports efficient panel processing. Those savings can disappear when the layout demands intensive manual insertion, unusual masking, selective soldering, rework, or a larger PCB.

The strongest cost drivers are:

  • Component count and package mix: automated SMT placement is usually more scalable than repeated manual insertion, lead forming, or hand soldering.
  • Board size and panel utilization: spreading a circuit over a larger one-sided board can reduce the number of units per panel and increase bare-board material cost.
  • Assembly sequence: mixed SMT and through-hole builds require more operations than SMT-only boards, even when all components occupy one side.
  • Tooling and soldering access: wave pallets, selective-solder fixtures, masking, or restricted nozzle access add setup and process time.
  • Inspection and test coverage: AOI, X-ray where applicable, in-circuit testing, functional testing, programming, and custom fixtures affect non-recurring and per-unit cost.
  • Volume and change frequency: prototypes absorb setup over few units, while stable repeat orders can distribute programming, stencil, tooling, and process-preparation costs more efficiently.

The lowest quoted board price is therefore not always the lowest finished PCBA cost. If a single-sided constraint increases board area, jumper count, hand work, or defect opportunities, a compact double-sided layout may produce a better total cost. Cost comparison should use the same quantity, test scope, sourcing responsibility, quality requirements, and delivery assumptions so that the two assembly options are evaluated on equal terms.

How Does Single Sided PCB Assembly Compare With Double Sided PCB Assembly?

Single sided PCB assembly usually offers a simpler production path, while double sided PCB assembly provides more placement area and routing freedom. The better option depends on whether the second populated surface removes more cost and risk than it adds.

Production factor Single sided assembly Double sided assembly
Component placement All components occupy one surface Components are placed on both surfaces
Typical process flow One SMT placement side, with optional THT operations Two placement sequences may be required
Board area May need more area for the same component count Can reduce footprint by using both surfaces
Handling and tooling Usually simpler Requires control of the first-side components during second-side processing
Inspection and repair Components are accessible from one side Access and traceability must cover both sides
Best fit Lower-density, cost-sensitive, serviceable products Compact, dense, interface-rich, or space-constrained products

A double-sided build does not automatically mean twice the assembly cost. Small passive components on the underside may allow a much smaller PCB, a shorter signal path, or a cleaner connector arrangement. Conversely, placing heavy or heat-sensitive parts on the second side can complicate reflow support and inspection.

The useful comparison is therefore process-specific. If all parts fit comfortably on one side with reliable solder access and acceptable board dimensions, single-sided assembly can keep production direct. If one-sided placement creates crowding, long routes, thermal concentration, too many jumpers, or difficult soldering, using both sides can make the finished PCBA easier to manufacture consistently.

Where Does Single Sided PCB Assembly Work Best—and Where Does It Fall Short?

Single sided PCB assembly works best in products with modest component density, uncomplicated interconnections, sufficient board area, and no strong need to minimize enclosure size. Common examples include simple power controls, indicator boards, appliance controls, relay boards, LED products, basic sensor interfaces, and low-complexity industrial electronics. The format is also useful when visible component identification and straightforward repair access matter.

Its limitations appear as the circuit becomes denser or more demanding. A one-sided component population can become restrictive when the product needs fine-pitch processors, large memory groups, many connectors, controlled-impedance interfaces, short high-current paths, extensive shielding, or concentrated thermal management. Forcing those functions onto one surface can enlarge the board or produce congested routing and uneven heat distribution.

Mechanical conditions matter as well. Tall components may conflict with the enclosure even if enough board area exists. Connectors may need fixed edge locations, displays or switches may have user-interface constraints, and heavy parts may require additional support. These factors can make a seemingly simple one-sided layout difficult to assemble or install.

The format is most successful when it follows the product’s real requirements rather than serving as an absolute design rule. Keeping one assembly side is worthwhile when it simplifies production without creating penalties elsewhere. When density, thermal performance, signal behavior, or enclosure limits become dominant, a double-sided or multilayer solution may deliver a more reliable and economical result.

How Are Single Sided PCB Assemblies Inspected and Tested?

Inspection and testing should verify both the general assembly quality and the features that are critical to the product’s function. Because components are concentrated on one side, visual access may be easier, but one-sided placement does not eliminate defects such as wrong parts, polarity errors, insufficient solder, bridging, lifted leads, contamination, or damaged through-hole barrels.

single sided PCB assembly
Optical inspection and electrical probing verify different aspects of the finished assembly.

The inspection route can include:

  • Incoming and bare-board checks for dimensions, finish, solder mask, markings, holes, and electrical continuity.
  • Solder-paste inspection for SMT builds where paste volume and alignment influence joint formation.
  • Automated optical inspection for component presence, orientation, polarity, placement, and visible solder conditions.
  • Visual inspection for through-hole fill, lead protrusion, solder bridges, flux residues, mechanical damage, and workmanship details not fully covered by AOI.
  • X-ray inspection when hidden joints or package geometry justify it; X-ray is not required merely because the assembly is single sided.
  • Electrical testing such as continuity, shorts testing, in-circuit testing, programming, or functional testing according to the agreed product requirements.

Inspection must match the technology on the board. A through-hole connector needs different acceptance evidence from a small SMT resistor, while a programmed controller requires more than a visual solder-joint check. Clear test limits, fixtures, firmware versions, and pass/fail conditions allow the finished units to be evaluated consistently across production lots.

FAQs About Single Sided PCB Assembly

Is a single sided PCB the same as single sided PCB assembly?

No. A single sided PCB has one conductive copper layer, while single sided PCB assembly means all mounted components occupy one side. A multilayer board can still use a one-sided component population.

Can SMT and through-hole parts be assembled on the same side?

Yes. SMT and through-hole parts can share one component side, but they normally require different placement and soldering operations. Their spacing and process order must allow each operation to be completed without damaging previously mounted parts.

Is single sided PCB assembly always cheaper?

No. It is often economical when it eliminates second-side processing without increasing board area or manual work. A double-sided assembly may cost less overall if it reduces PCB size, jumpers, routing difficulty, special tooling, or rework.

Can a multilayer PCB use single-sided component assembly?

Yes. Copper-layer count and component-side count are separate choices. A multilayer PCB may keep every component on one surface to simplify assembly or meet mechanical requirements.

What files are needed to quote a single sided PCB assembly?

A usable quotation package normally includes PCB fabrication data, a fabrication drawing or stackup requirements, the BOM, centroid or pick-and-place data for SMT parts, assembly drawings, polarity and revision information, and the required inspection, programming, and test scope.

Single sided PCB assembly is most valuable when one populated surface simplifies production without forcing extra board area, jumpers, or manual operations. EBest Circuit can review customer-released PCB and assembly data, manufacture the bare boards, source approved components, complete SMT and through-hole assembly, and perform agreed inspection and testing. To discuss a prototype or repeat-production build, contact sales@bestpcbs.com.

You may also like

Selective Wave Soldering: Avoid Mixed-Assembly Rework
Monday, August 10th, 2026

Selective wave soldering targets programmed through-hole joints instead of exposing the full board underside. It can protect reflowed components and improve consistency, but only when the layout, nozzle access, production volume, and acceptance criteria support the process.

selective wave soldering
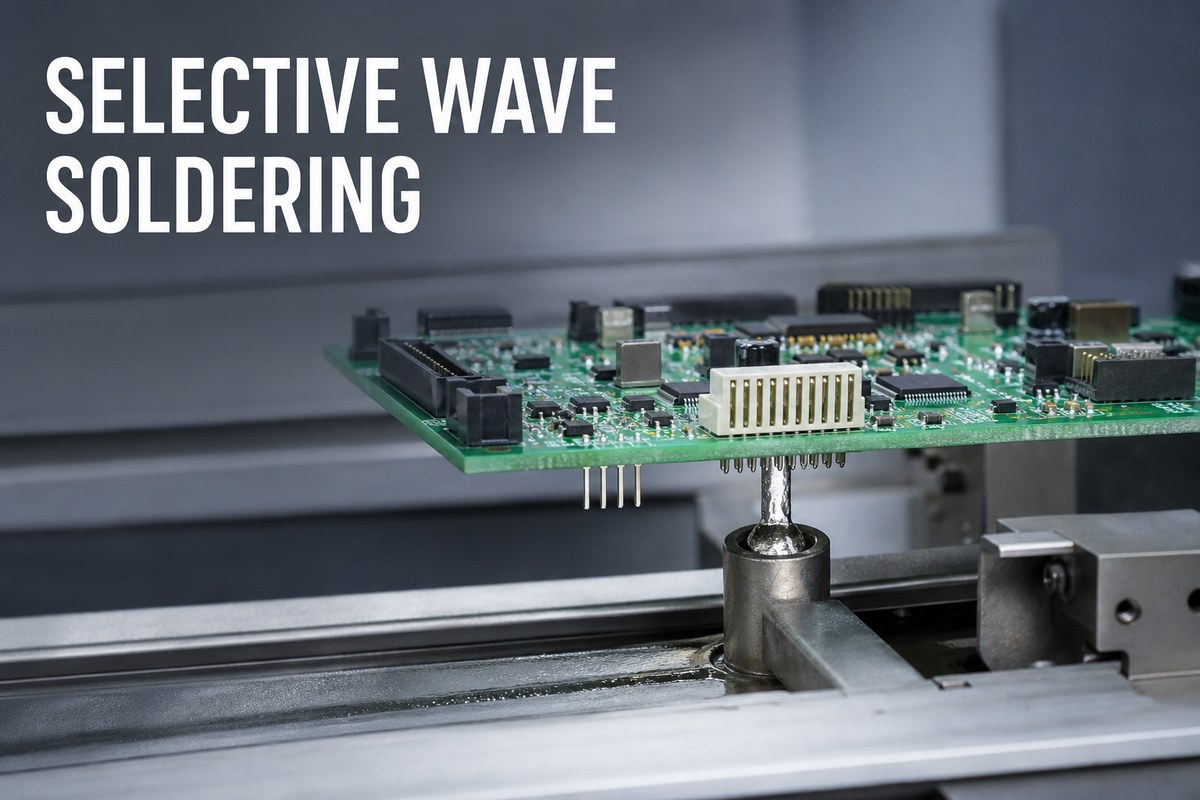
Selective wave soldering for targeted through-hole joints on a mixed-technology PCB assembly.

What Is Selective Wave Soldering?

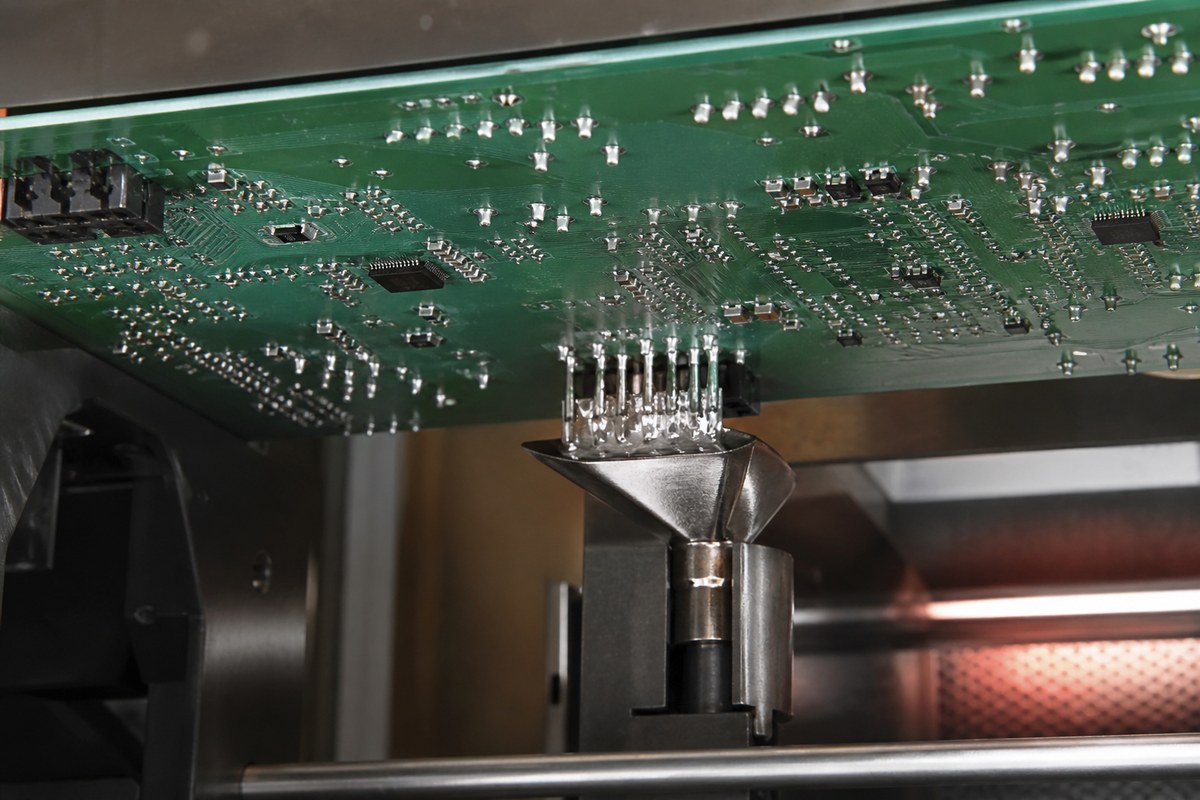
Selective wave soldering is an automated process that applies flux, heat, and molten solder to chosen plated through-hole joints. A small nozzle or mini-wave reaches the target area without deliberately exposing the full board underside.

It is often used after SMT reflow to solder connectors, relays, transformers, terminals, and switches. Compared with extensive hand soldering or full-wave exposure, it can reduce masking, operator variation, and touch-up.

The process still needs enough nozzle clearance, flux coverage, and heat transfer. The real question is whether the released assembly provides a stable and inspectable process window.

When Does Selective Wave Soldering Prevent Rework?

Selective wave soldering is most useful when a board has reflowed SMDs on the bottom side but only a limited number of through-hole joints.

It may reduce rework when:

  • Bottom-side SMDs are close to through-hole joints.
  • Heat-sensitive parts should avoid a full solder wave.
  • High-pin-count connectors need repeatable soldering.
  • Hand soldering would add too much variation.
  • Product variants require different through-hole locations.

It is not always the lowest-cost choice. Full wave soldering may suit a through-hole-heavy board, while controlled hand soldering may suit a simple prototype. Early supplier review helps identify access or layout problems before production.

Selective Soldering vs Wave Soldering

Both processes create through-hole joints, but they expose the PCB differently. The best choice depends on layout, volume, setup cost, cycle time, and rework risk.

FactorSelective solderingWave soldering
ContactTargeted jointsFull underside
Best fitMixed SMT/THTTHT-heavy boards
SetupProgram and nozzleProfile and pallet
SpeedSlower pathFaster for many joints
Main riskAccess and cycle timeHeat, masking, rework

Compare total cost, not only unit price. Include programming, pallets, first-article inspection, manual touch-up, and scrap risk. A selective process may cost more per cycle but less overall if it prevents masking and rework.

How Does the Selective Wave Soldering Process Work?

The selective wave soldering process normally includes five stages:

  • Flux: A controlled amount reaches the selected joints.
  • Preheat: Heat activates the flux and reduces thermal shock.
  • Soldering: A programmed nozzle contacts each joint or joint group.
  • Cooling: Joints solidify without disturbance.
  • Inspection: Results are checked against the approved criteria.

Board thickness, copper distribution, surface finish, hole fit, alloy, flux, and component mass all affect the process window. A generic temperature or dwell time cannot fit every PCB.

A first article should prove that the selected settings work on the actual assembly. Approved programs, materials, and inspection criteria should then remain under revision control.

selective wave soldering
A localized solder nozzle targets a selected through-hole connector area.

Selective Wave Soldering Design Rules

Selective wave soldering design rules should protect nozzle access and support consistent heat transfer.

Review before PCB release:

  • Nozzle access: Nearby parts must not block the target joint.
  • Clearance: Keep enough space from SMDs, shields, and tall bodies.
  • Lead protrusion: Allow solder contact without creating shorting risk.
  • Hole fit: Support component insertion and solder flow.
  • Pad and mask: Promote wetting without encouraging bridges.
  • Thermal balance: Review joints connected to planes or heavy copper.
  • Panel access: Rails and tooling must not block the path.
  • Inspection access: Finished joints must be assessable.

Missing these checks can lead to blocked nozzles, connector bridging, or poor fill on high-mass pins. The result may be manual rework, new tooling, or a PCB revision.

EBest Circuit (Best Technology) can review manufacturability and assembly access within the agreed production scope. The customer remains responsible for component approval, circuit function, safety spacing, and the released design.

How Do You Prevent Selective Soldering Defects?

Selective soldering defects should be traced to the actual board condition and process variable. Increasing heat without finding the cause may fix one joint and damage another.

DefectCommon causeCheck
BridgingTight spacing or excess solderMask, path, withdrawal
Poor barrel fillLow heat or high thermal massPreheat, dwell, hole fit
Non-wettingOxidation or weak flux actionStorage, finish, flux
IciclesPoor withdrawal or excess contactPath, dwell, nozzle
Solder ballsExcess flux or splashingFlux, preheat, setup
Pad damageExcess heat or repeated repairProfile and repair history

A practical validation plan includes:

  • Confirm the BOM, PCB revision, drawing, and program.
  • Run a first article with production materials and equipment.
  • Inspect ordinary and high-thermal-mass joints.
  • Agree on barrel fill, bridging, residue, and damage criteria.
  • Record approved settings and permitted touch-up.
  • Revalidate after significant material or design changes.

Inspection must follow the customer’s specified workmanship and contractual requirements. The assembler should provide evidence for the agreed PCBA scope, while the customer owns final product acceptance.

selective wave soldering
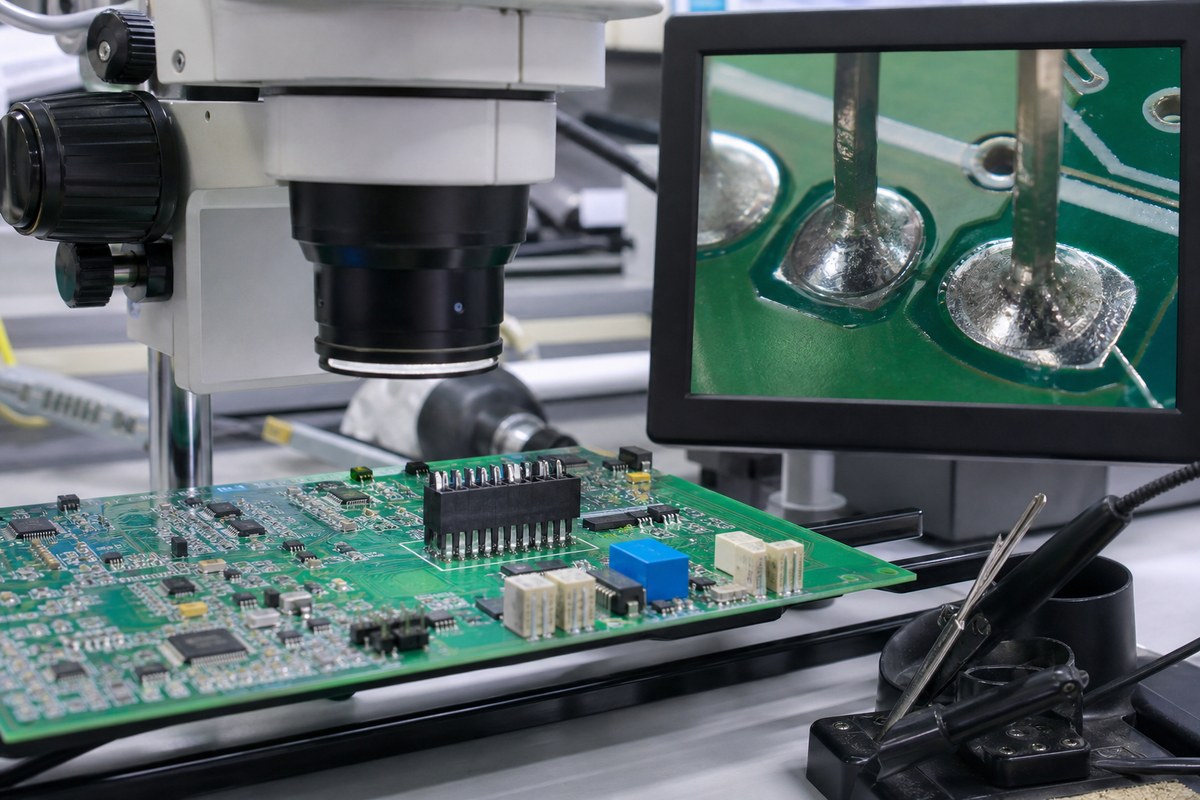
Inspection helps verify solder-joint quality against the agreed acceptance criteria.

What Should a Selective Wave Soldering RFQ Include?

An incomplete RFQ can hide access conflicts, difficult connectors, and special inspection needs. These discoveries often lead to quotation changes later.

Send the following files and requirements:

  • Gerbers, drill data, and fabrication drawing.
  • BOM with approved manufacturer part numbers.
  • Placement data and assembly drawings.
  • Panel requirements and relevant component datasheets.
  • Order quantity, repeat demand, and product variants.
  • Solder alloy, cleaning, and material restrictions.
  • Workmanship, hole-fill, and inspection requirements.
  • Test, traceability, and packaging instructions.

Also identify areas where touch-up is prohibited or downstream coating creates a special constraint. A complete package helps the supplier compare selective soldering, wave soldering, hand soldering, or a hybrid route on the same released scope.

A Mixed-Technology PCB Assembly Example

Consider a double-sided SMT assembly with a multi-pin connector, power terminal, and relay added after reflow. Bottom-side passives sit near the connector, while the terminal connects to a large copper area.

Full wave soldering may require a pallet to protect the SMDs. Hand soldering may add variation and labor. A selective-soldering review would instead check:

  • Nozzle access around the connector pins.
  • Extra heat demand at the power terminal.
  • Relay clearance and lead protrusion.
  • First-article results at both normal and difficult joints.

If the process window is stable, selective soldering may reduce masking and touch-up. If the nozzle cannot reach the connector, the layout, tooling, or soldering method should change before production.

This is a manufacturing example, not a claim about a specific customer project. The final decision depends on the actual PCB, BOM, volume, and acceptance requirements.

How Can EBest Support Selective Wave Soldering?

EBest Circuit (Best Technology) supports customers within the PCB and PCBA manufacturing scope. Support may include:

  • PCB manufacturability and assembly-access review.
  • PCB fabrication and revision control.
  • BOM review and sourcing coordination.
  • SMT and agreed through-hole assembly.
  • Selective-soldering feasibility review.
  • First-article inspection and agreed testing.
  • Required traceability and production records.

The customer retains responsibility for circuit design, component approval, firmware, regulatory requirements, certification, and final product validation. Responsibilities should be defined by the quotation, released files, and approved inspection or test requirements.

Selective Wave Soldering FAQs

Is selective wave soldering the same as selective soldering?
It is a common selective-soldering method that uses a localized solder wave or nozzle. Because “selective soldering” can also describe other localized methods, the RFQ should name the intended process.

Can selective soldering replace wave soldering on every PCB?
No. Nozzle access, joint count, cycle time, thermal mass, volume, and cost may make wave soldering or another process more suitable.

Does selective wave soldering eliminate hand soldering?
It can reduce manual work when joints are accessible and the program is stable. Blocked or very low-quantity joints may still require an approved alternative.

What causes insufficient hole fill during selective soldering?
Common causes include inadequate heat, high copper mass, poor hole fit, weak solderability, flux problems, or an unstable nozzle path.

What files are needed for a selective-soldering quotation?
Provide PCB fabrication data, BOM, assembly files, component details, quantities, panel information, inspection criteria, and test or traceability requirements.

Need help deciding whether selective wave soldering fits your mixed-technology PCBA? Send your released PCB files, BOM, quantities, and acceptance requirements to sales@bestpcbs.com for a manufacturing review and quotation.

You may also like