PCB manufacturing PCB manufacturing
Home > Blog

PCB Bow & Twist: IPC Limits, Measurement & Calculation Guide

September 18th, 2026

PCB bow and twist are forms of PCB warpage that can affect solder paste printing, component coplanarity, connector fit, automated handling, and final mechanical assembly. The percentage may look small, but on a large or thin PCB, even a fraction of one percent can produce several millimeters of displacement.

For engineers and buyers, the practical questions are therefore not only “Is the board warped?” but how the deformation is classified, how it is measured, which IPC requirement applies, and whether the board meets the agreed flatness specification.
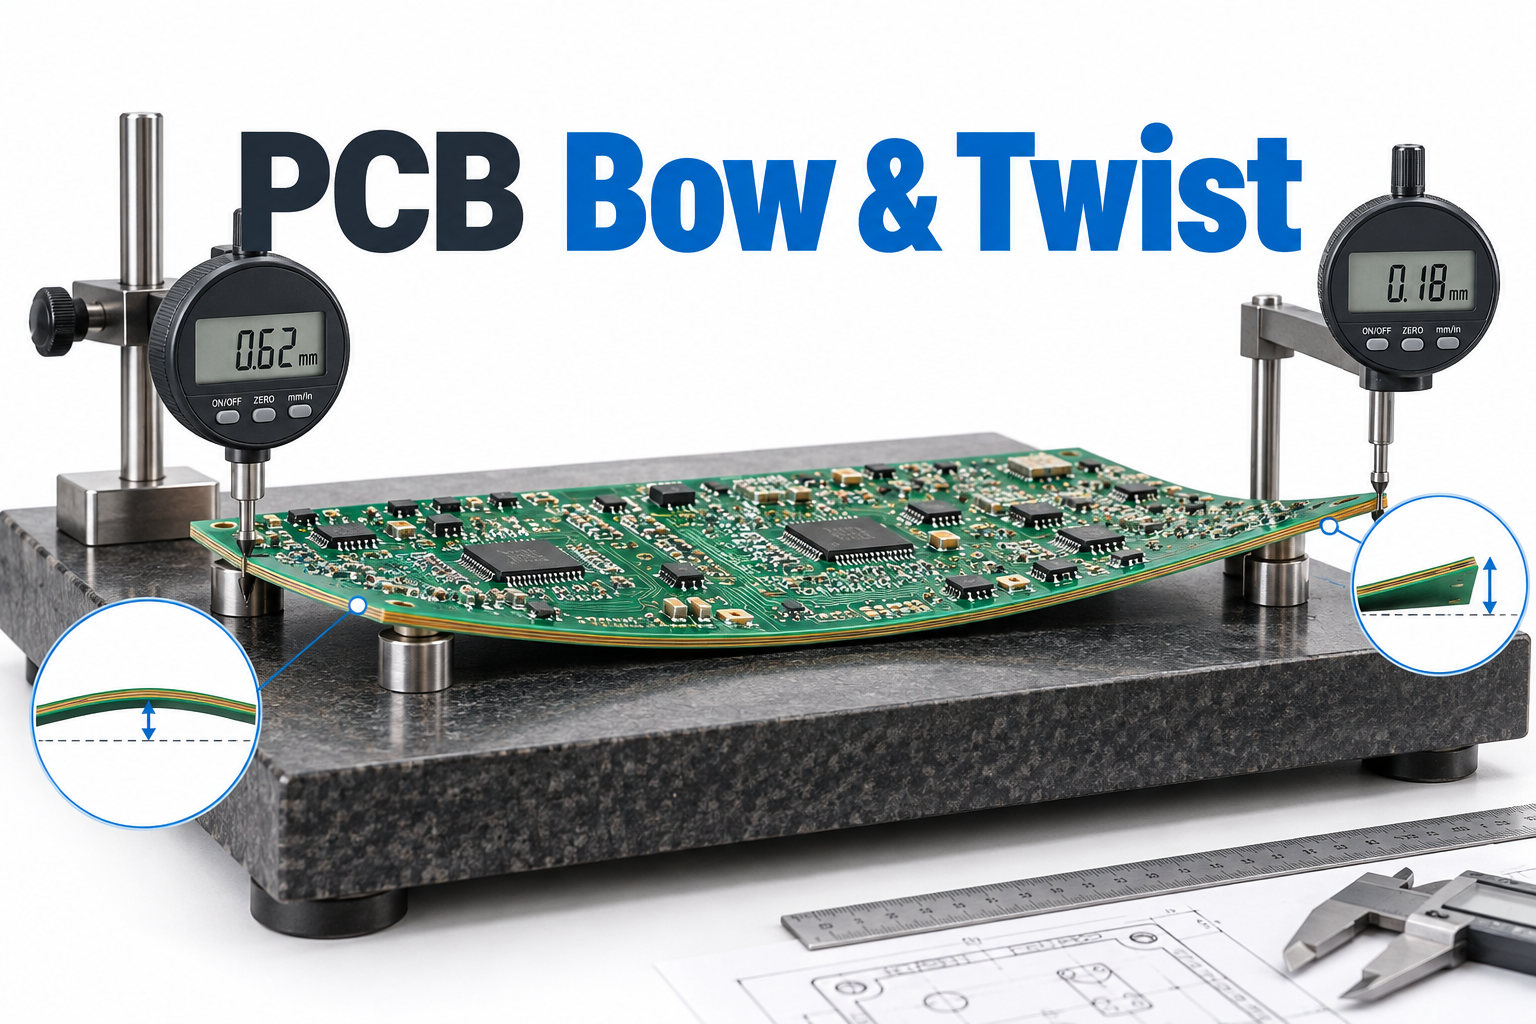
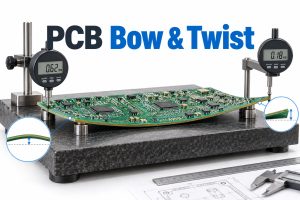
PCB Bow and Twist measurement on a precision surface plate

Key Takeaways

  • PCB bow is a curved deformation, while PCB twist is a diagonal deformation that lifts one corner out of the plane formed by the other three corners.
  • IPC-6012F specifies a default maximum bow and twist of 0.75% for printed boards using surface-mount components and 1.5% for other printed boards, unless procurement documentation specifies otherwise.
  • IPC-TM-650 2.4.22 is the key test method for determining bow and twist percentage on rigid printed boards, rigid portions of rigid-flex boards, and multiple-board panels.
  • For bow, the measured gap is divided by the corresponding board length or width. For production-method twist, the lifted-corner gap is divided by twice the board diagonal.
  • A 200 × 300 mm SMT PCB with a 0.75% limit allows 1.50 mm bow across the 200 mm direction, 2.25 mm across the 300 mm direction, and approximately 5.41 mm raised-corner gap for the IPC production twist method.
  • Asymmetric stackups, uneven copper distribution, material construction, lamination conditions, and later thermal or mechanical stress can all contribute to PCB warpage.
  • The IPC 0.75% value is an acceptance limit, not necessarily the optimum flatness target for every assembly.

What Are PCB Bow and Twist?

PCB bow and twist are two different forms of deviation from flatness. PCB bow is roughly cylindrical or spherical curvature in which the four corners of a rectangular board remain in one plane, while twist occurs along a diagonal so that one corner lies outside the plane formed by the other three.

Characteristic PCB Bow PCB Twist
Typical shape Arc, hump, or shallow dome Propeller-like diagonal distortion
Corner condition Four corners can remain coplanar One corner lifts relative to the other three
Main measurement reference Board length and width Board diagonal
Production measurement Maximum gap along an edge direction Raised-corner gap

A board can also show a combination of bow and twist. In that case, simply measuring the highest point from a tabletop does not necessarily produce the correct IPC percentage.

The test setup and calculation method need to match the type of deformation being evaluated.
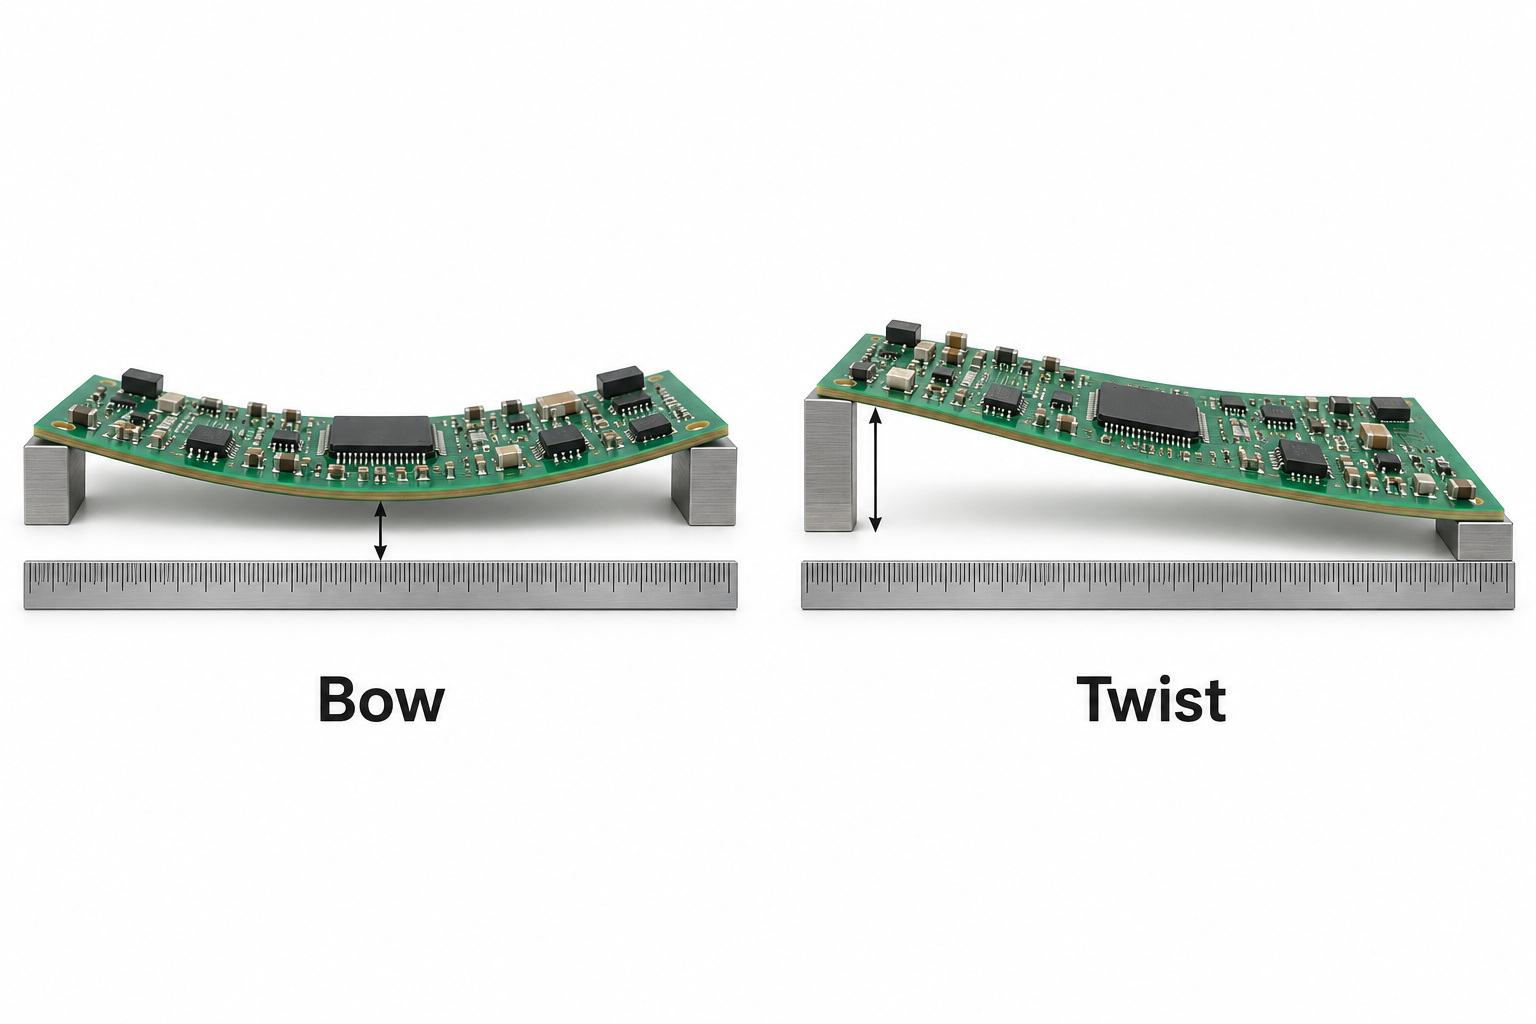
PCB bow compared with PCB twist deformation

What Is the IPC Standard for PCB Bow and Twist?

IPC-6012F specifies that, unless otherwise stated in the procurement documentation, finished rigid printed boards designed in accordance with IPC-2221 have a maximum bow and twist of 0.75% when surface-mount components are used and 1.5% for other printed boards.

Board Application Default IPC-6012F Maximum
Printed board using surface-mount components 0.75%
Other printed boards 1.50%

These percentages are default acceptance requirements, not universal design targets. A customer drawing, procurement specification, or product-specific requirement can call for tighter flatness.

Finished boards are also assessed in their delivered form. If boards are supplied in pallet arrays for assembly, the bow and twist requirement for the array may be agreed separately between the user and supplier.

IPC-TM-650 2.4.22 vs 2.4.22.1: What Is the Difference?

IPC-TM-650 2.4.22 and 2.4.22.1 sound nearly identical, but they report flatness differently.

Test Method Main Purpose Result
IPC-TM-650 2.4.22C Bow and twist of rigid boards, rigid portions of rigid-flex, and multiple-board panels Percentage
IPC-TM-650 2.4.22.1C Maximum vertical displacement of panels, finished rigid boards, and rigid portions of rigid-flex Displacement in mm/in

Method 2.4.22 includes production Go/No-Go procedures for bow and twist, plus a more precise referee procedure for twist. It uses a precision surface plate, feeler or pin gauges, measuring devices, and, for the referee method, additional support and dial-indicator equipment.

Method 2.4.22.1 instead records the maximum vertical displacement of an unrestrained specimen. Its scope applies to laminates at least 0.5 mm [0.020 in] thick and can also be used after etching or thermal stress when agreed between user and supplier.

These methods should therefore not be treated as interchangeable calculations.

How Do You Measure PCB Bow?

PCB bow is measured by placing the board on a precision flat surface with the convex side facing upward and measuring the gap created by the curvature. A bow and twist PCB check should classify the deformation before selecting the measurement method.

For the IPC-TM-650 2.4.22 production method:

  1. Measure the board length L and width W.
  2. Place the board on a precision surface plate, convex side upward.
  3. For the edge being checked, apply enough pressure at both corners of that edge to bring them into contact with the datum surface.
  4. Insert a feeler or pin gauge between the PCB and surface plate.
  5. Determine the largest gauge that fits for the length and width directions.
  6. Record these measurements as RL and RW.
  7. Calculate bow percentage separately for length and width.

IPC calculates bow in the corresponding board direction. The denominator is not automatically the PCB diagonal.

This distinction matters because using the diagonal would produce a lower calculated percentage and could incorrectly classify an out-of-tolerance board as acceptable.
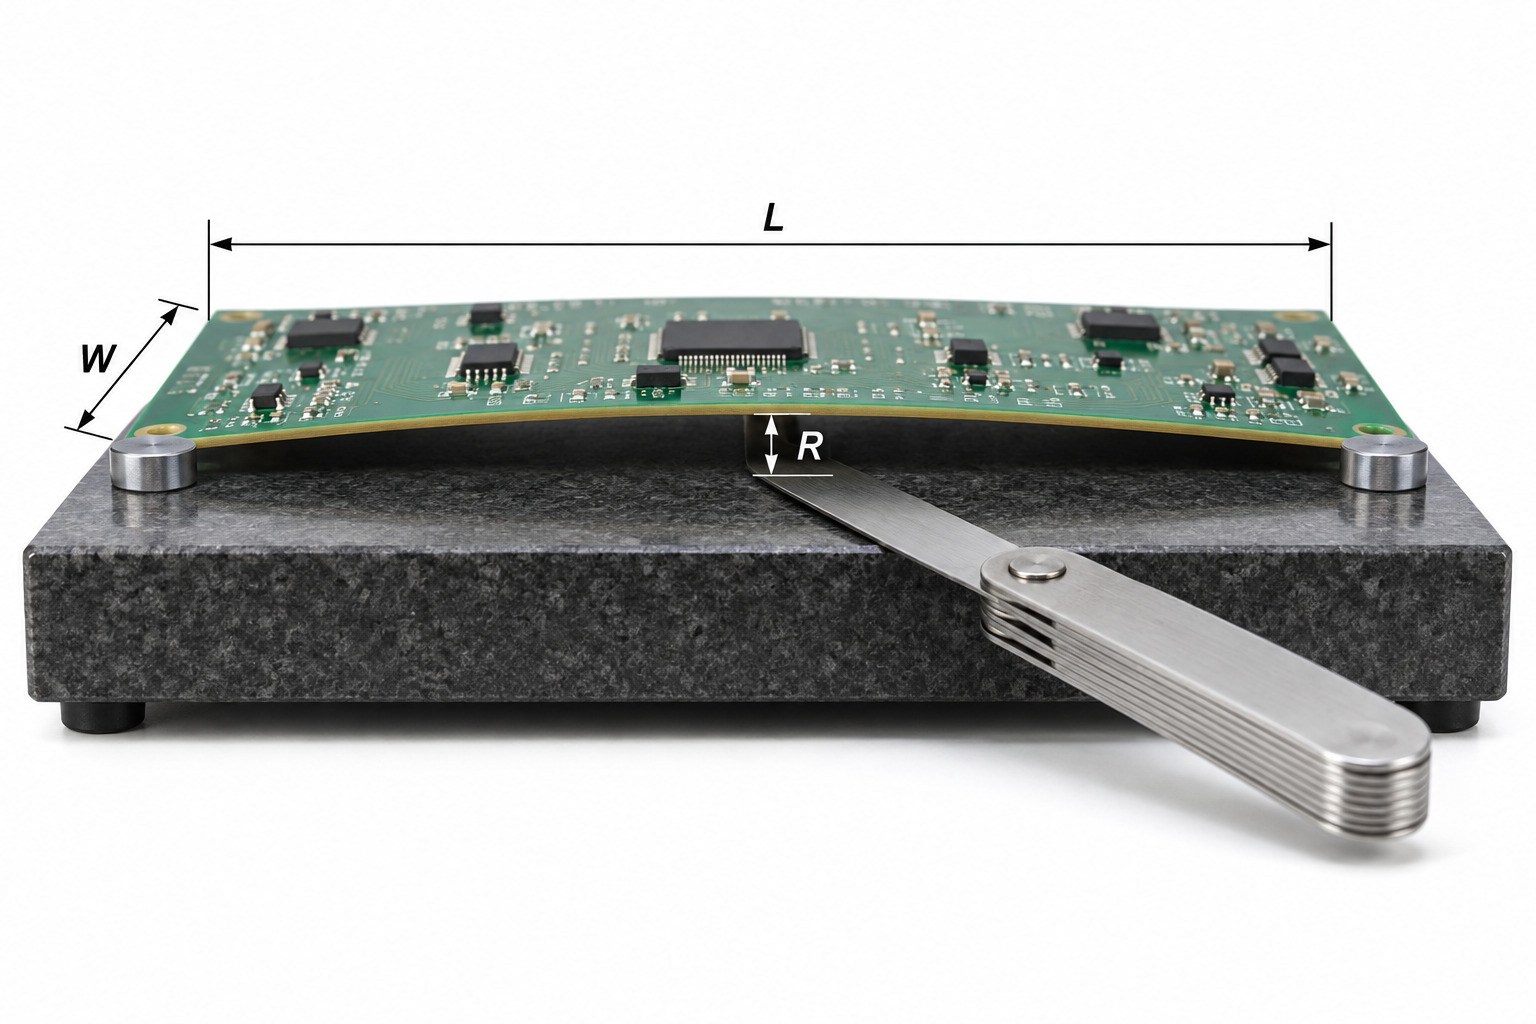
PCB bow measurement using a precision surface plate and feeler gauge with length width and gap dimensions

How Do You Measure PCB Twist?

For production testing, PCB twist is measured by placing three corners of the board against a flat datum surface and measuring the gap beneath the remaining lifted corner.

The IPC-TM-650 2.4.22 procedure is:

  1. Measure the board diagonal and record it as D.
  2. Place the PCB on the surface plate.
  3. Position it so that three corners contact the surface.
  4. If necessary, restrain only one corner to establish three-point contact.
  5. Insert a feeler or pin gauge under the remaining lifted corner.
  6. Find the largest gauge that fits without lifting the other three corners.
  7. Record that gap as R.
  8. Calculate the twist percentage.

The production formula contains a factor of two because constraining one corner against the surface plate approximately doubles the observed vertical twist deflection.

If three corners cannot be brought into contact by restraining only one corner, the referee method should be used instead of forcing the production procedure.
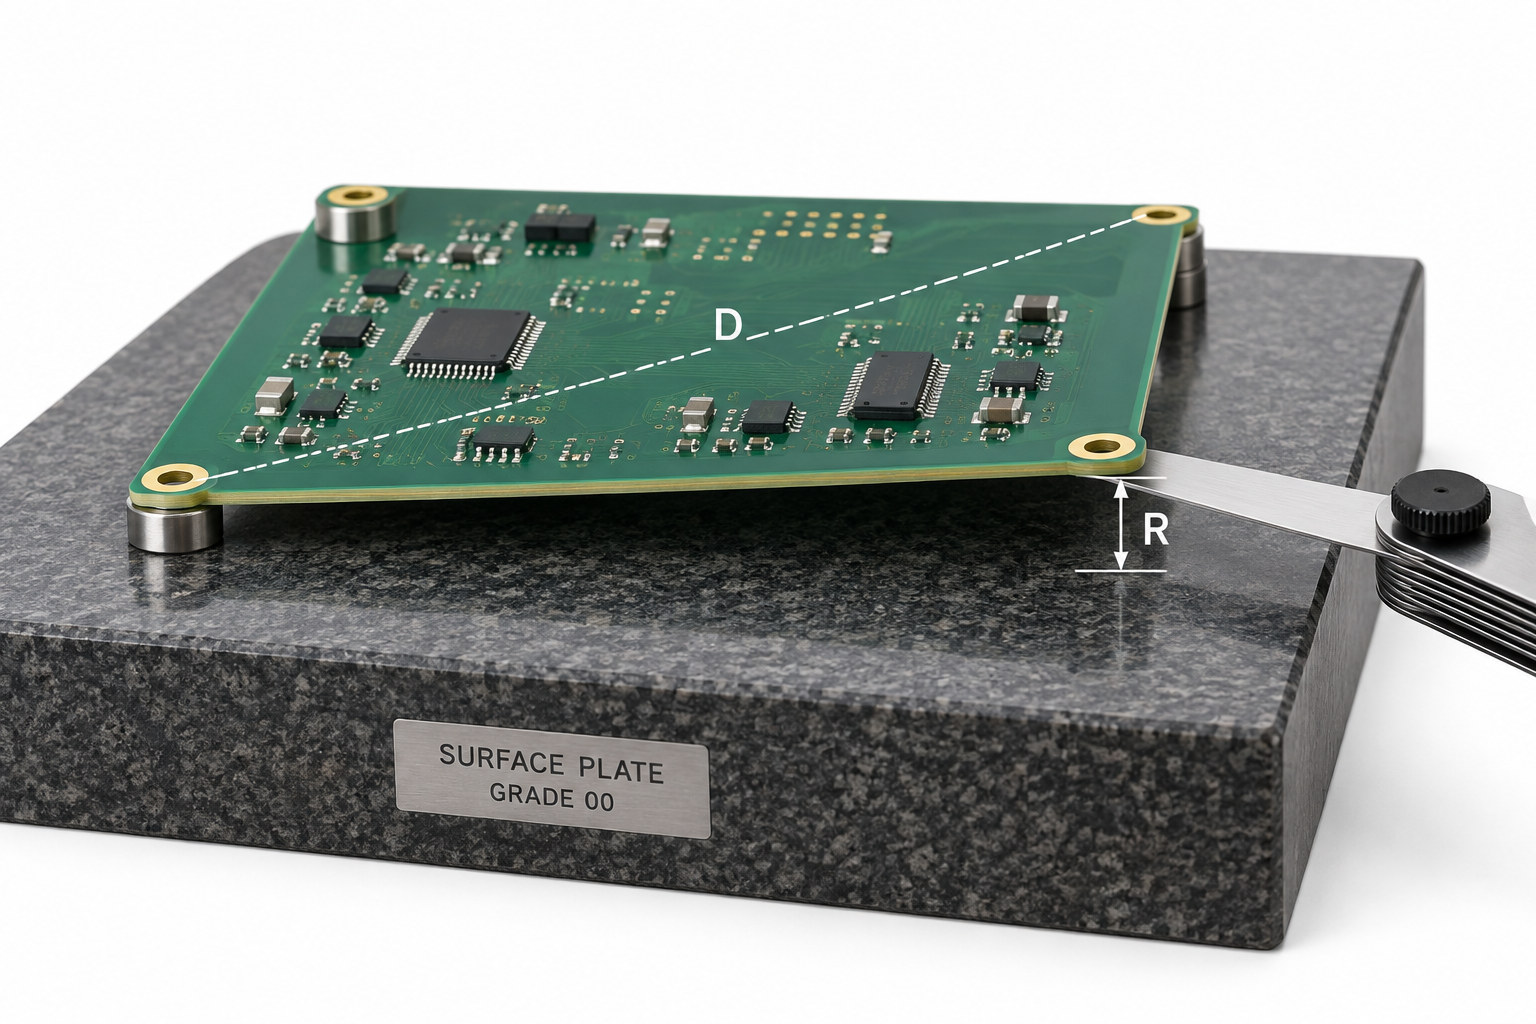
PCB twist measurement showing board diagonal D and raised corner gap R on a precision surface plate

What Is the PCB Bow and Twist Formula?

IPC-TM-650 2.4.22 uses different formulas for bow and production-method twist. A PCB bow and twist calculator must use the correct board direction or diagonal for the deformation being measured.

Bow in the length direction:

BowL (%) = (RL / L) × 100

Bow in the width direction:

BowW (%) = (RW / W) × 100

Where:

  • RL = maximum measured gap in the length direction
  • RW = maximum measured gap in the width direction
  • L = PCB length
  • W = PCB width

Twist — production method:

Twist (%) = (R / (2 × D)) × 100

Where:

  • R = maximum gap under the raised corner
  • D = PCB diagonal

The factor of two should not be removed when using this IPC production measurement method.

For a rectangular PCB, the diagonal is:

D = √(L² + W²)

How Do You Calculate PCB Bow and Twist?

Consider a 200 × 300 mm PCB that will use SMT components. Using the default IPC-6012F limit of 0.75%, the maximum allowable production-measurement gaps can be calculated before inspection.

The PCB bow and twist percentage must always be evaluated against the board dimensions and the agreed acceptance limit.

PCB dimensions

  • Width = 200 mm
  • Length = 300 mm
  • Bow/twist limit = 0.75%

First calculate the board diagonal:

D = √(200² + 300²) = 360.56 mm

The allowable gaps are:

Calculation Formula Maximum Gap
Bow across 200 mm direction 200 × 0.75% 1.50 mm
Bow across 300 mm direction 300 × 0.75% 2.25 mm
Twist production gap 2 × 360.56 × 0.75% 5.41 mm

Now assume the measured 300 mm-direction bow gap is 1.80 mm:

Bow = (1.80 / 300) × 100 = 0.60%

That result is below 0.75%.

If the measured lifted-corner gap for twist is 4.00 mm:

Twist = (4.00 / (2 × 360.56)) × 100 ≈ 0.55%

That result is also below 0.75%.

This example shows why a physical gap in millimeters cannot be judged by itself. The same displacement produces a different bow or twist percentage depending on board dimensions.

What Causes PCB Bow and Twist?

PCB bow and twist usually result from uneven internal stress rather than one isolated defect. The source can enter during design, material preparation, fabrication, or later thermal processing.

Evaluating bow and twist in PCB production starts with identifying where uneven stress entered the process.

PCB Design

Common design-related contributors include asymmetric stackups, unequal copper weights above and below the centerline, large differences in local copper density, large cutouts, and panel breakaway areas that do not reflect the copper distribution of the finished board.

Materials

Glass-fabric orientation, core and prepreg construction, CTE mismatch, mixed laminate systems, and moisture condition can affect dimensional stability.

PCB Manufacturing

Press conditions, incomplete cure, incorrect prepreg construction, uneven heating or cooling, solder-mask cure, and hot-air solder leveling can introduce or release stress.

Assembly and Handling

Mechanical loading, storage, reflow, fixtures, conveyor support, and asymmetric component mass can further change the board shape.

A useful way to think about these mechanisms is that some stress is built into the PCB during lamination, while other deformation is introduced later by handling or thermal processing.

Why Does Copper Distribution Affect PCB Warpage?

Copper and dielectric materials respond differently to temperature and processing stress, so an unbalanced copper pattern can create unequal forces through the PCB thickness.

The problem can occur in two ways:

  • Layer-to-layer imbalance: one side of the stack has heavier copper or larger plane areas than its mirrored layer.
  • Local imbalance: one region contains dense copper while another region contains very little copper.

During multilayer pressing, copper density also affects resin flow and local pressure. During later thermal cycles, different copper distributions can contribute to unequal expansion and stress.

A symmetrical stackup with similar copper weights and coverage on corresponding layers reduces this risk. Panel breakaway areas should also avoid extreme copper-density differences compared with the PCB itself.

Copper filling or thieving may help balance sparse areas, but it should still respect electrical clearance, impedance, creepage, and signal-integrity requirements.
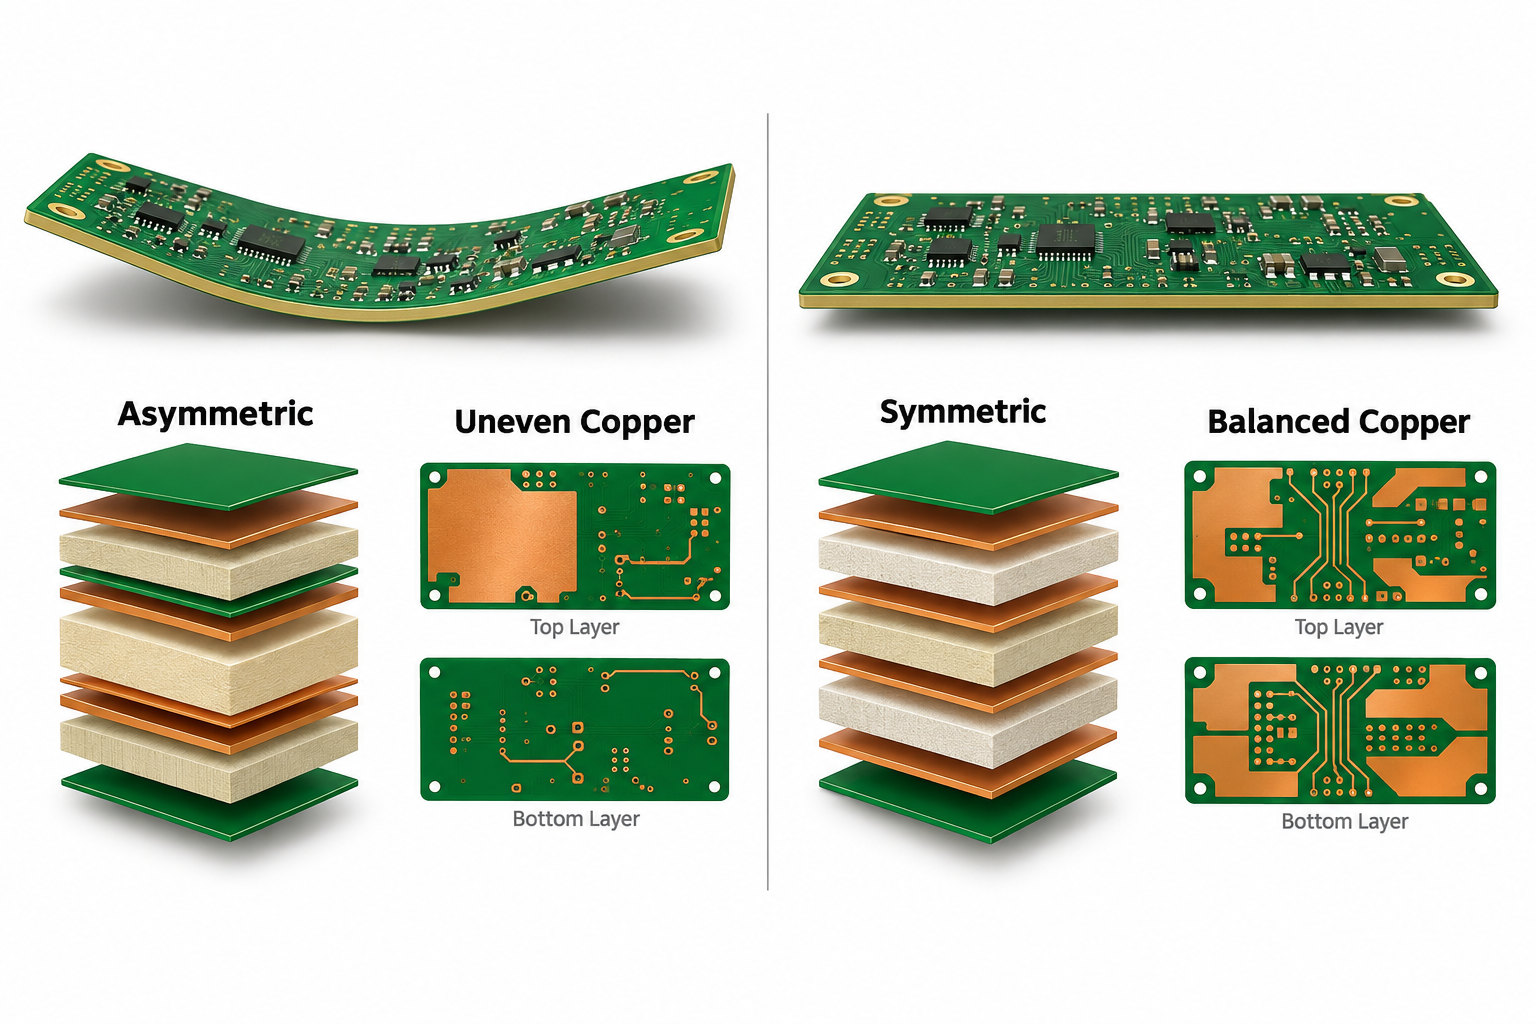
PCB warpage comparison showing asymmetric stackup and uneven copper versus symmetric stackup and balanced copper

How Can PCB Bow and Twist Be Reduced Before Fabrication?

The most effective time to control PCB warpage is before the stackup and panel design are frozen.

Useful DFM checks include:

  • Keep the multilayer stackup symmetric around the centerline.
  • Use matching copper weights on mirrored layers where practical.
  • Balance copper coverage across opposing sides.
  • Review large copper-free or low-density regions.
  • Keep core and prepreg construction mechanically balanced.
  • Review glass orientation where material construction makes it relevant.
  • Consider board thickness relative to size and mechanical support.
  • Balance copper in panel rails and breakaway areas.
  • Review mixed-material stackups for CTE and lamination compatibility.
  • Define any tighter flatness requirement on the drawing before production.

For EBest Circuit projects, bow-and-twist risk can be reviewed during DFM together with stackup construction, copper distribution, panelization, material selection, and finished thickness.

How Is Bow and Twist Controlled During PCB Manufacturing?

Manufacturing control focuses on preventing uneven stress from being built into or released from the panel.

Important process controls include:

  • Laminate and prepreg storage
  • Glass direction and ply construction
  • Controlled lamination temperature and pressure
  • Resin-flow and cure control
  • Symmetrical panel construction
  • Copper plating balance
  • Solder-mask and legend curing
  • HASL or other high-temperature processing
  • Panel support during handling
  • Controlled cooling
  • Final flatness inspection

Lamination is particularly important because once intrinsic deformation is locked into the multilayer structure, later flattening may not provide a permanent correction.

Final inspection should be performed on the board in the required delivered form and against the applicable customer or IPC limit.

When Should a PCB Use a Tighter Flatness Limit Than IPC 0.75%?

A tighter requirement may be appropriate whenever the standard 0.75% bare-board limit does not provide enough mechanical or assembly margin.

Examples include boards with:

  • Large BGA or fine-pitch area-array packages
  • Long board-edge connectors
  • Press-fit connector fields
  • Tight card-guide or chassis interfaces
  • Thin, large-format PCBs
  • High-density SMT on both sides
  • Precision optical or sensor assemblies
  • Customer-defined coplanarity requirements

The correct tighter value depends on the product. It should not be assumed that every BGA board requires 0.5%, 0.3%, or another generic number.

IPC-6012F allows procurement documentation to specify requirements other than the default 0.75% or 1.5% limits.

For tight-flatness projects, the designer and PCB manufacturer should agree on the measurement method, delivery form, panel condition, temperature condition, and acceptance limit before fabrication.

Does IPC-TM-650 Bow and Twist Apply to an Assembled PCBA?

IPC-TM-650 2.4.22 is primarily a bare printed-board flatness test. Its scope covers individual rigid boards, rigid portions of rigid-flex boards, and multiple-board panels, but it does not address all special conditions of populated assemblies such as component weight, placement, edge supports, and connectors.

An assembled PCBA can behave differently because reflow temperature, component packages, heat sinks, connectors, fixtures, and solder joints all influence deformation.

For temperature-dependent board flatness, separate methods may be used to evaluate local board shape through a simulated reflow cycle. These do not replace room-temperature bow and twist inspection of the bare PCB.

Bare-board bow/twist and assembled-PCBA warpage should therefore be treated as related but different engineering problems.

FAQ About PCB Bow and Twist

1. What is the maximum PCB bow and twist allowed by IPC?
IPC-6012F specifies a default maximum of 0.75% for printed boards using surface-mount components and 1.5% for other printed boards, unless procurement documentation requires a different limit.

2. How is PCB bow percentage calculated?
PCB bow percentage is calculated from the maximum measured gap relative to the corresponding board length or width.

3. How is PCB twist percentage calculated?
PCB twist percentage is calculated from the raised-corner gap and the PCB diagonal using the IPC-TM-650 production method.

4. Is PCB bow the same as PCB twist?
No. Bow is a curved deformation in which the four corners can remain coplanar, while twist is a diagonal deformation that raises one corner relative to the other three.

5. What commonly causes excessive PCB warpage?
Asymmetric stackups, uneven copper distribution, material construction, lamination stress, incomplete cure, mechanical handling, and later thermal processes can all contribute.

6. Can a customer specify a tighter bow and twist limit?
Yes. A customer can define a tighter requirement in the procurement documentation, and that agreed requirement takes precedence over the general IPC default for the project.

PCB bow and twist should be controlled from stackup design through final inspection rather than treated only as an end-of-line flatness problem. Symmetry, copper balance, material construction, lamination, panel design, and thermal processing all influence the final result.

For PCB projects with tight flatness requirements, EBest Circuit can review the Gerber files, stackup, copper distribution, panelization, finished thickness, assembly requirements, and target bow/twist limit before production. Send the project data to sales@bestpcbs.com for DFM review.
You may also like

PMIC Power Management Integrated Circuit: Functions, Types & PCB Design Guide

September 18th, 2026

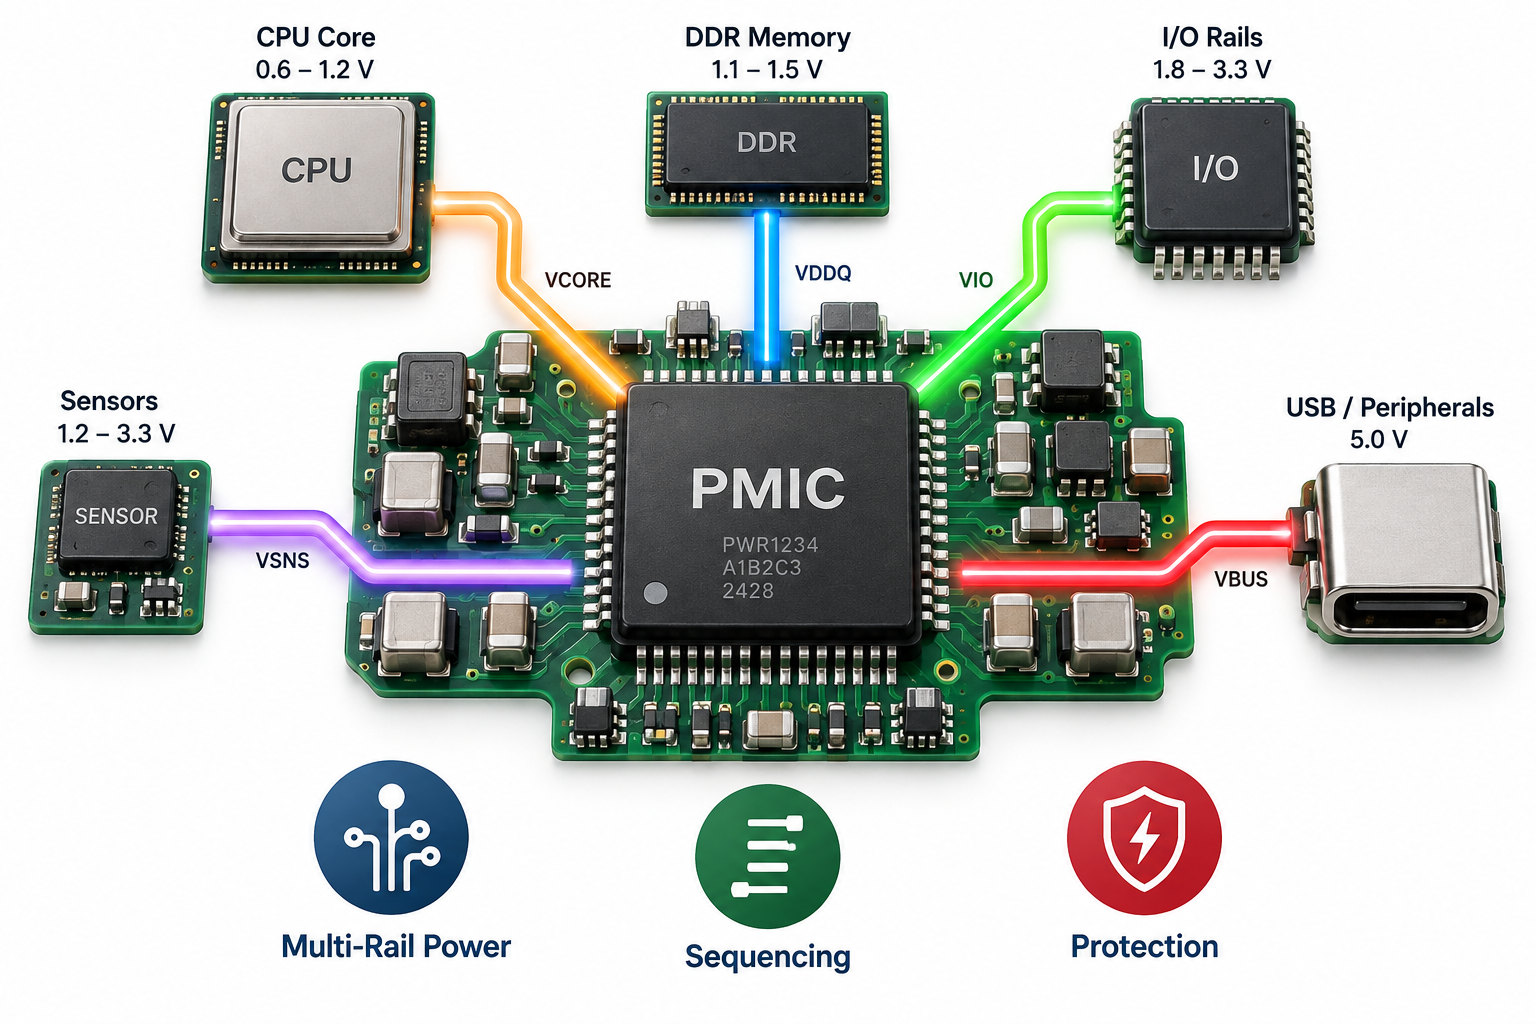
A PMIC, or Power Management Integrated Circuit, manages the different voltage rails required by processors, memory, communication devices, sensors, and other electronic circuits. Instead of building every rail from separate regulators and control ICs, a PMIC can combine several power functions into one coordinated device.

This approach is increasingly common in embedded systems, edge AI hardware, automotive electronics, IoT products, industrial equipment, and other boards with complex power trees. However, using a PMIC does not eliminate power-design work. Rail sequencing, current capacity, external components, PCB layout, thermal management, assembly, and testing still determine whether the final system operates reliably.

PMIC power management integrated circuit supplying CPU DDR I/O sensors and USB power rails

Key Takeaways

  • PMIC stands for Power Management Integrated Circuit, a chip that can generate, regulate, sequence, monitor, and protect multiple power rails in one electronic system.
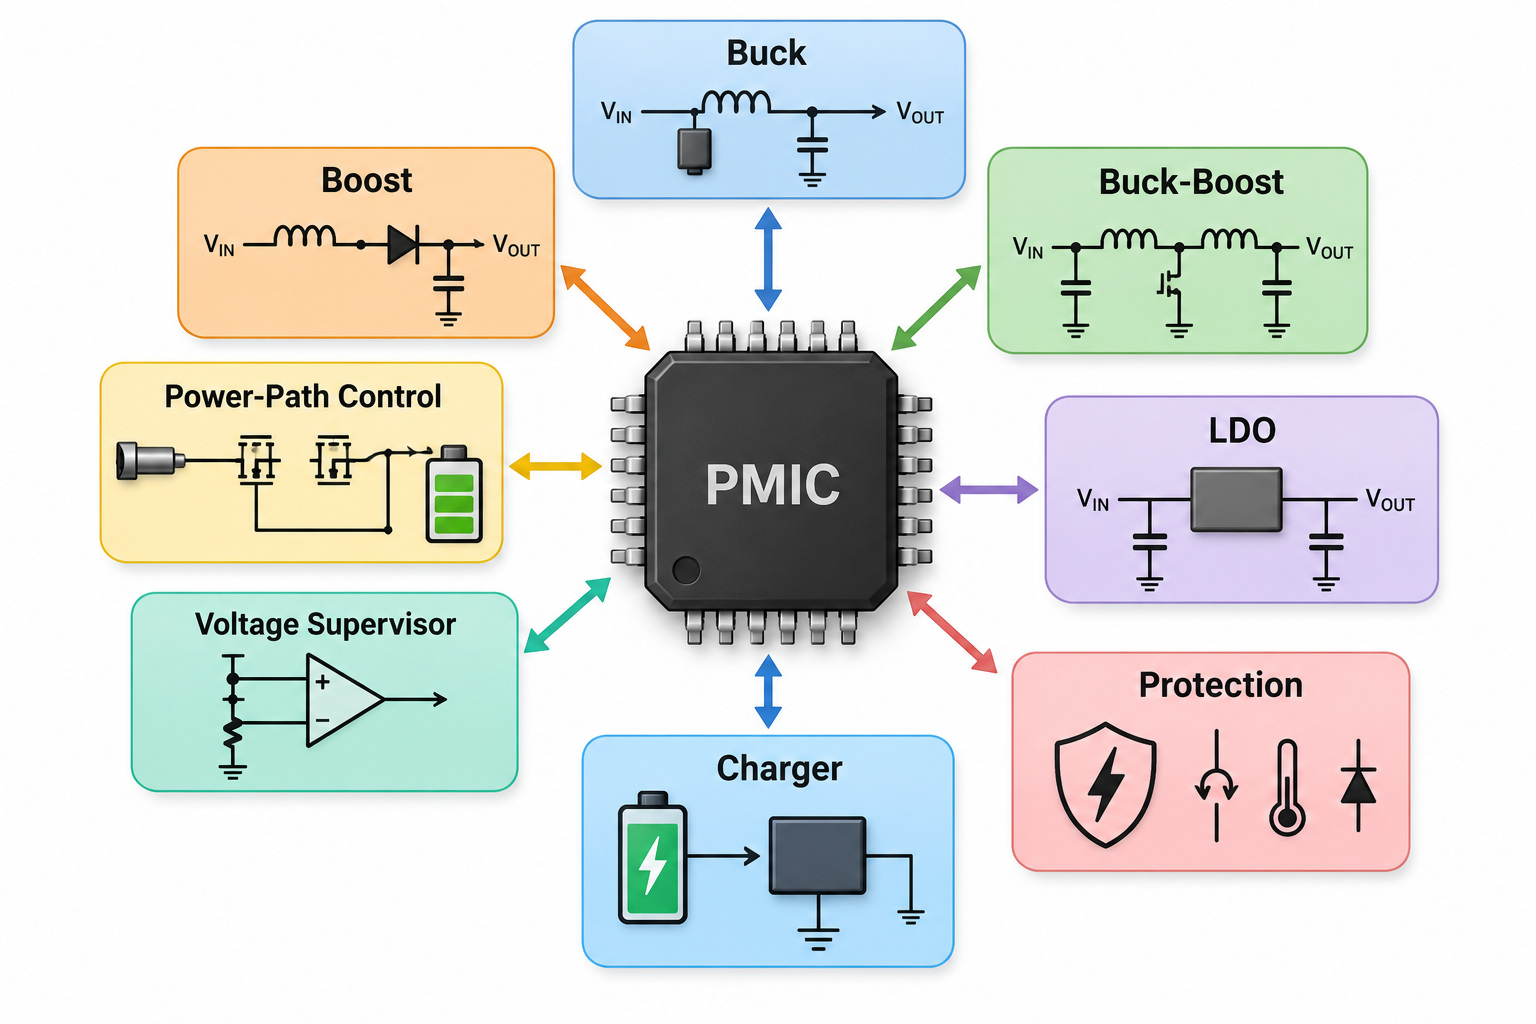
  • A PMIC may integrate buck converters, boost converters, buck-boost converters, LDOs, battery charging, power-path control, sequencing, monitoring, and fault protection.
  • PMICs are especially useful when processors, FPGAs, DDR memory, sensors, and peripherals require multiple voltages with controlled startup and shutdown timing.
  • A PMIC is not the same as a single voltage regulator or DC-DC converter. It usually coordinates several power functions rather than controlling only one rail.
  • PMIC selection should consider input voltage, rail count, output current, efficiency, quiescent current, switching frequency, sequencing, digital interfaces, package, and thermal limits.
  • PCB layout strongly affects PMIC performance. High-current loops, switching nodes, inductors, feedback routing, decoupling, grounding, and thermal vias require careful placement.
  • Most PMICs still need external components such as inductors and capacitors, even when several regulators and control functions are integrated into one IC.

What Is a PMIC Power Management Integrated Circuit?

A PMIC, or Power Management Integrated Circuit, is an IC designed to generate, regulate, distribute, sequence, monitor, and protect the power rails used by an electronic system.

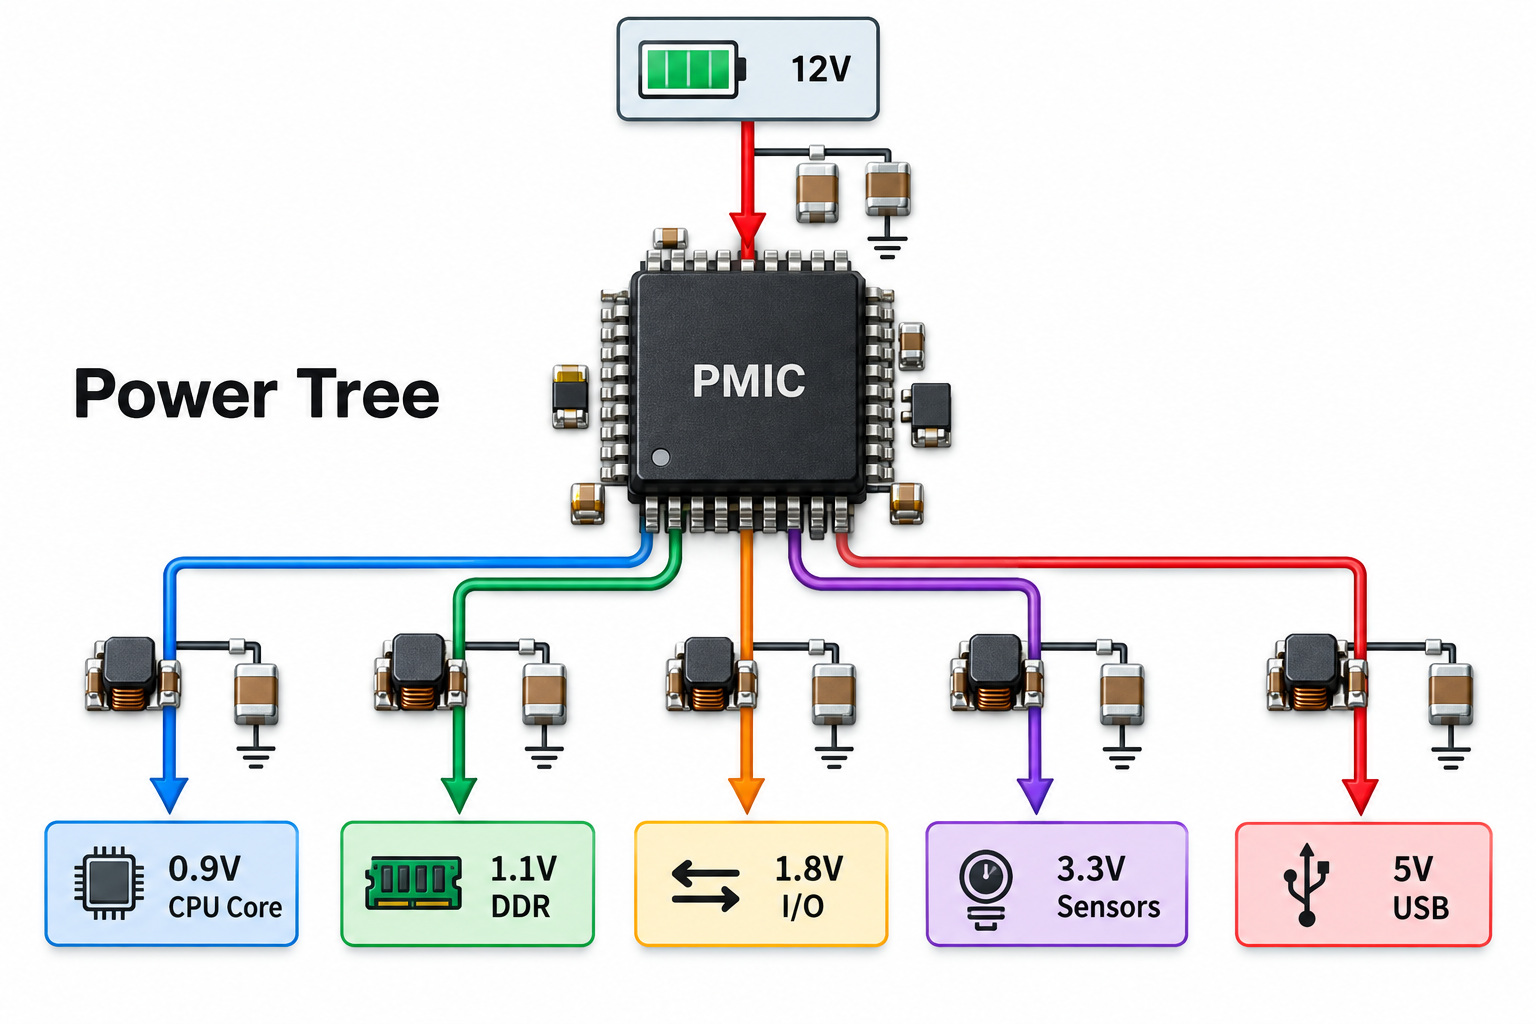
A simple product may need only one regulated voltage, but a modern processor-based PCB can require several rails such as:

  • 0.8–1.0 V processor core
  • 1.1 V memory
  • 1.8 V I/O
  • 3.3 V peripherals
  • 5 V USB or auxiliary circuits

Instead of using one independent regulator for every rail, a PMIC can combine several power converters and control functions in one package.

The term PMIC can also be used broadly by semiconductor distributors for many power-management IC categories. In practical embedded design, however, “a PMIC” usually refers to a more integrated device that manages several power domains or system-level power functions.

What Functions Can a PMIC Integrate?

A PMIC can combine several power-conversion and control blocks that would otherwise require multiple ICs and supporting components.

PMIC Function What It Does
Buck converter Steps voltage down efficiently
Boost converter Steps voltage up
Buck-boost converter Regulates when input may be above or below output
LDO Provides low-noise regulated voltage
Sequencer Controls rail startup and shutdown order
Battery charger Manages charging current and voltage
Power-path controller Selects or manages available power sources
Voltage supervisor Monitors rails and generates reset/fault signals
Load switch Connects or disconnects downstream loads
Protection circuit Handles overcurrent, overvoltage, undervoltage, or thermal faults

Not every PMIC includes all of these functions. A processor-oriented PMIC may focus on several buck converters, LDOs, sequencing, and monitoring, while a battery-powered device may place more emphasis on charging, power-path control, and low quiescent current.

This integration reduces the number of separate control ICs, but external inductors, capacitors, resistors, and sometimes MOSFETs may still be required.

PMIC functional blocks including buck boost buck-boost LDO charger power path supervisor and protection

How Does a PMIC Work in a Multi-Rail Power Tree?

A PMIC sits between the main power source and the different voltage domains required by the system.

A simplified power tree might look like:

12 V / 5 V / Battery Input → PMIC → 0.9 V CPU core / 1.1 V DDR memory / 1.8 V I/O / 3.3 V sensors and peripherals / 5 V USB or auxiliary load

Each rail can have different voltage, current, noise, and startup requirements. The PMIC coordinates these rails instead of treating them as independent power supplies.

A switching converter is normally used where efficiency matters, while an LDO may supply a lower-current rail that needs less noise. Some designs also allow rails to be reprogrammed through I²C, SPI, or stored configuration.

For processor and FPGA projects, EBest Circuit can review the power tree together with PMIC placement, external power components, current paths, and PCB stackup during DFM before fabrication.

PMIC multi-rail power tree showing 12 V input and CPU DDR I/O sensor and USB outputs

How Does PMIC Power Sequencing Work?

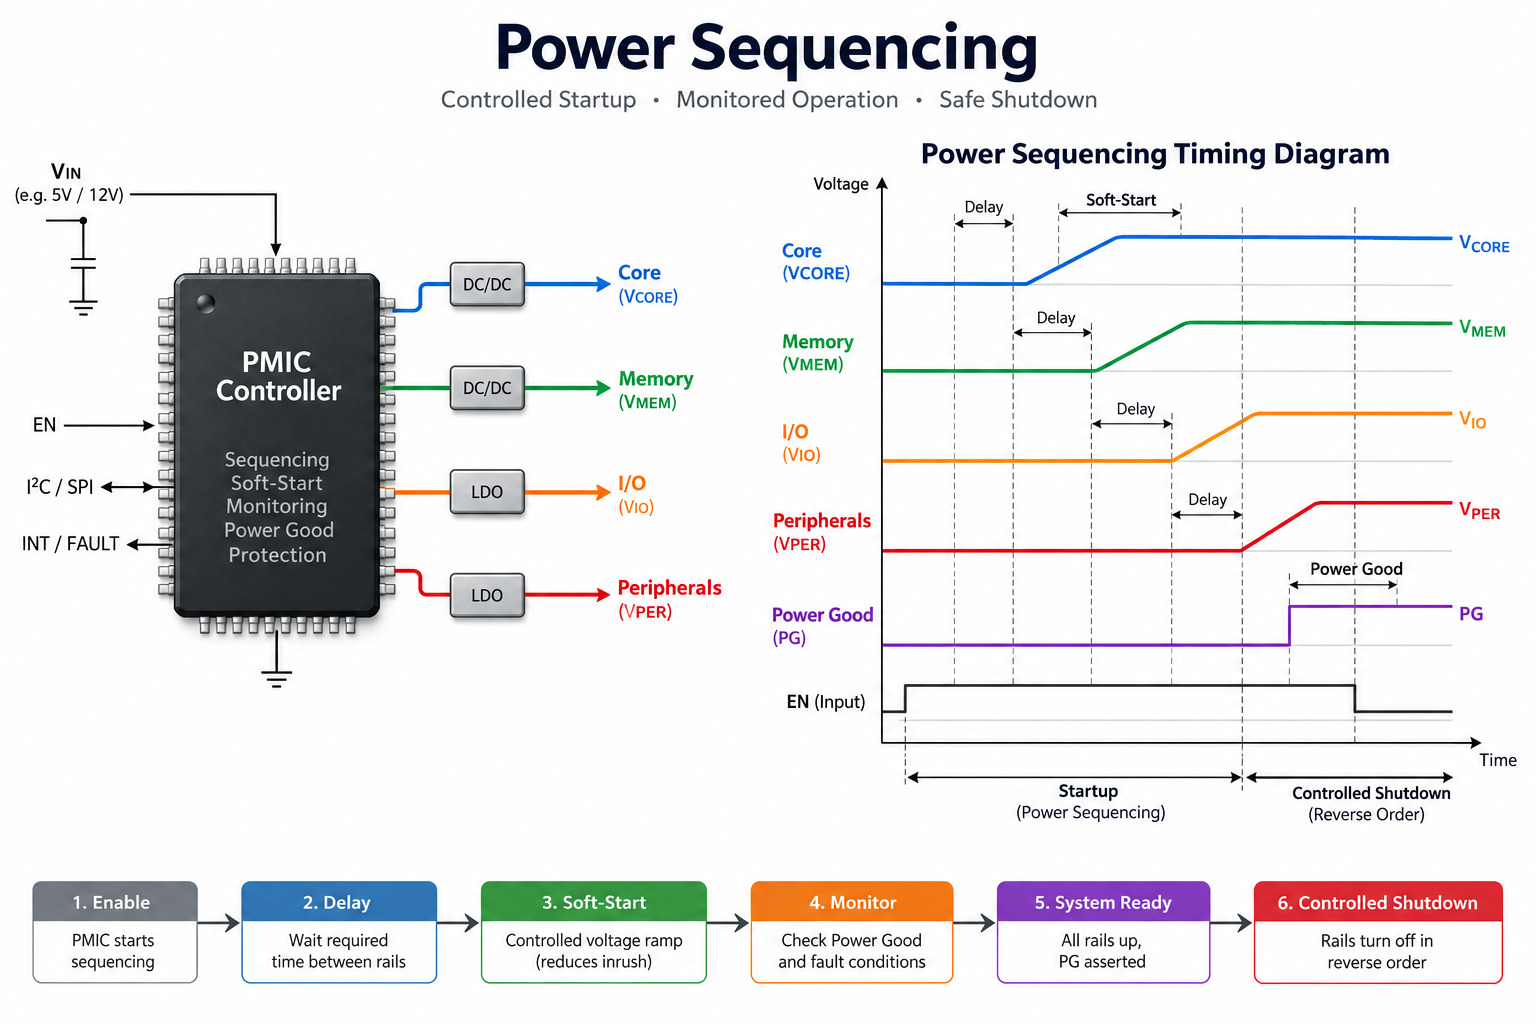
Power sequencing controls the order and timing in which voltage rails turn on and off.

Processors, FPGAs, DDR memory, and other complex ICs may require one rail to stabilize before another starts. Applying the wrong voltage first can cause excessive current, startup failure, latch-up, or undefined device behavior.

A simplified startup sequence might be:

Core rail → Memory rail → I/O rail → Peripheral rail

A PMIC may control this using:

  • Programmable delay times
  • Soft-start ramps
  • Power-good signals
  • Enable outputs
  • Voltage monitoring
  • Reset generation
  • Fault shutdown
  • Controlled reverse sequencing during power-down

Some PMICs use fixed factory sequencing, while others allow the sequence to be programmed through registers or nonvolatile configuration.

Power-down behavior matters as much as startup. Certain processors require rails to fall in a defined order so that I/O pins, memory, or analog sections are not left biased incorrectly during shutdown.

PMIC power sequencing timing diagram with core memory I/O peripheral rails soft start delay power good and shutdown

PMIC vs Voltage Regulator vs DC-DC Converter: What Is the Difference?

A voltage regulator or DC-DC converter normally focuses on one power-conversion function, while a PMIC can coordinate several power rails and supervisory functions.

Feature PMIC Voltage Regulator DC-DC Converter
Typical rail count Multiple Usually one Usually one
Voltage regulation Yes Yes Yes
Buck/boost conversion Often several Device dependent Main function
Sequencing Often Usually limited Usually limited
Monitoring Often integrated Basic or limited Basic or limited
Battery management Possible Rare Rare
Digital programming Often available Less common Device dependent
System-level control Strong Limited Limited

An LDO is a voltage regulator. A buck converter is a DC-DC regulator. Both may be part of a PMIC.

The distinction is therefore mainly about integration and system coordination, not whether the IC can regulate voltage.

A design with one 3.3 V rail may not need a PMIC at all. A processor board with six rails, sequencing, reset logic, fault monitoring, and low-power modes is a much stronger PMIC application.

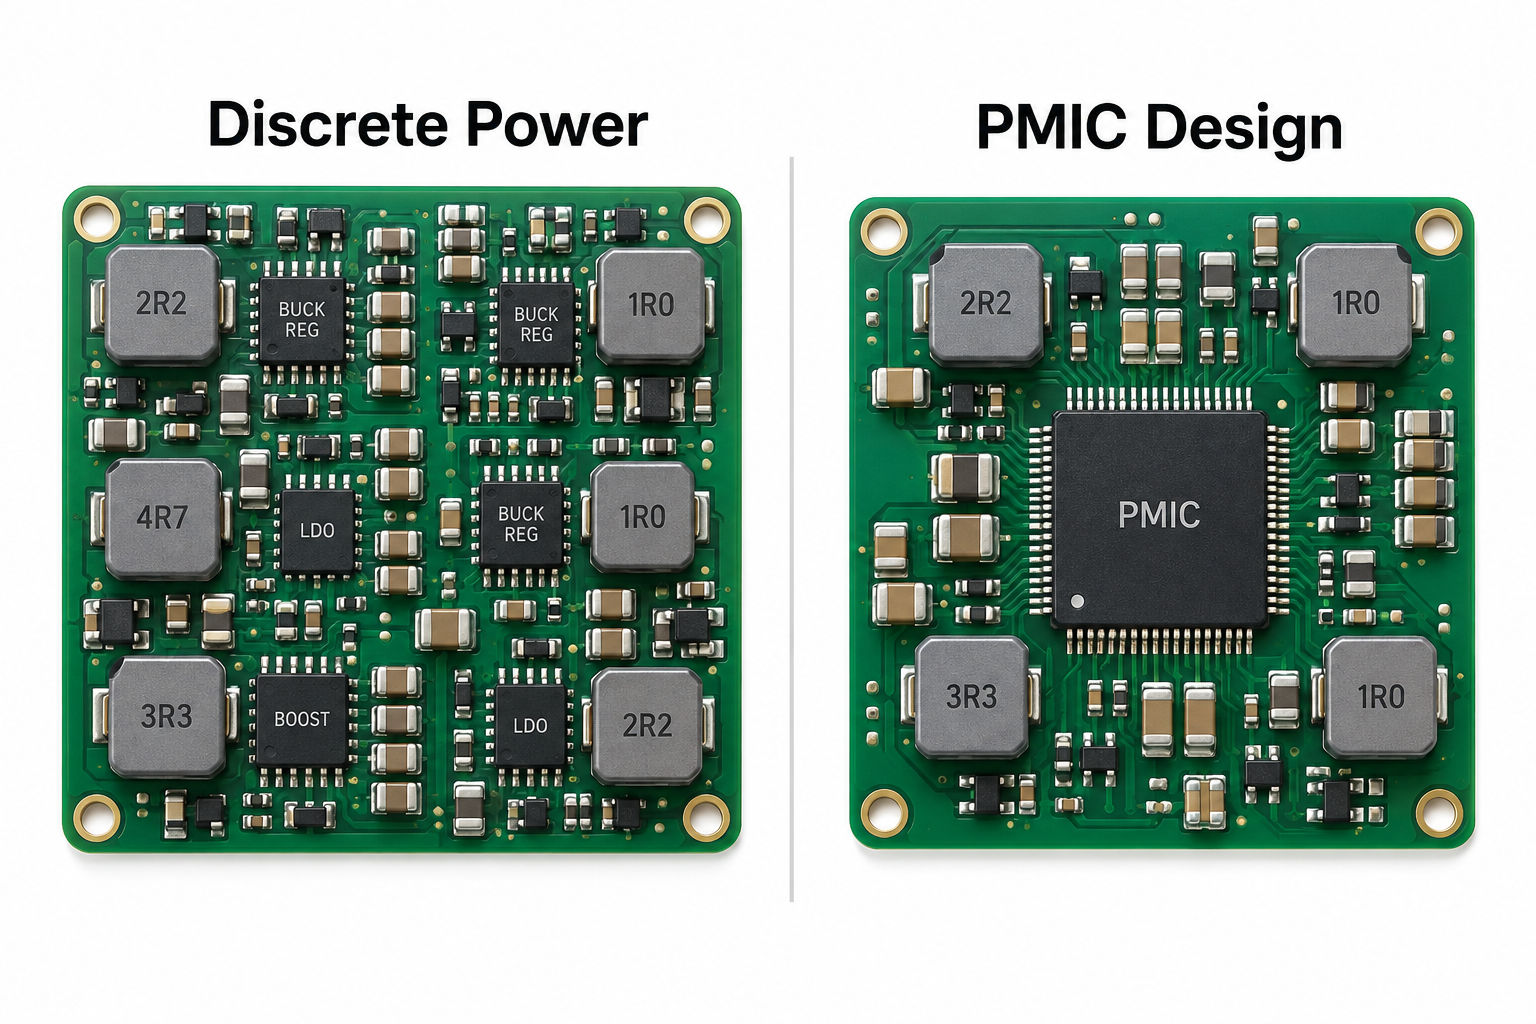
PMIC vs Discrete Power Design: When Does Integration Make Sense?

A PMIC becomes more attractive as the number of power rails and coordination requirements increase.

PMIC advantages include:

  • Smaller PCB area
  • Fewer separate control ICs
  • Integrated sequencing
  • Central fault monitoring
  • Programmable rail control
  • Reduced system-level design complexity
  • Coordinated low-power modes

A discrete design can still be the better choice when:

  • Only one or two rails are needed
  • Rail requirements change frequently
  • Different regulator vendors must be second-sourced
  • Heat needs to be distributed across the PCB
  • One rail requires an unusual converter topology
  • Independent replacement or qualification matters

A PMIC can also create sourcing concentration because several rails depend on one component. If that device becomes unavailable, replacing it may require more redesign than replacing one discrete regulator.

The decision should therefore consider not only board area and BOM count, but also lifecycle, sourcing, thermal distribution, and firmware configuration.

Discrete power design compared with integrated PMIC design on PCB

Key Specifications When Selecting a PMIC

Selecting a PMIC starts with the complete power tree, not simply the number of output channels. Input conditions, rail voltage, peak current, transient response, efficiency, sequencing, thermal limits, and control interfaces should all be checked against the processor and system requirements.

The ranges can vary significantly between PMIC families. For example, TI’s TPS65219-Q1 accepts up to 5.5 V, integrates 3 buck converters and 4 LDOs, provides up to 3.5 A from its highest-current buck, and switches at up to about 2.3 MHz. ST’s STPMIC1L also accepts 2.8–5.5 V, provides two buck converters rated up to 2 A, and operates at 2 MHz.

Specification Check Item Typical PMIC Specifications
Input voltage range Normal input, tolerance, startup and transient conditions STPMIC1L: 2.8–5.5 V; TPS65219-Q1: up to 5.5 V
Output rail count Number of buck, boost and LDO rails required TPS65219-Q1: 3 buck + 4 LDO
Output voltage range CPU core, DDR, I/O and peripheral voltages TPS65219-Q1: 0.6–3.4 V; STPMIC1L BUCK1: 0.5–4.2 V depending on mode
Output current Continuous, peak and startup current on each rail TPS65219-Q1: 3.5 A + 2 A + 2 A buck capability
Voltage accuracy Processor/DDR rail tolerance over line, load and temperature STPMIC1L buck regulation: typically around the ±1% to ±1.5% class, depending on rail and condition
Efficiency Efficiency at real operating loads, not only peak value Modern buck stages commonly operate in the 80–90%+ range, depending on VIN, VOUT and load
Quiescent current Standby power and battery-life impact TPS65219-Q1: about 250 µA typical
Switching frequency Inductor size, ripple, EMI and switching loss STPMIC1L: 2 MHz; TPS65219-Q1: up to about 2.3 MHz
Sequencing Power-up/down order, delay, ramp and power-good behavior Programmable sequencing is available on many processor PMICs
Protection OCP, OVP, UVLO, thermal shutdown and fault reporting Feature set varies by PMIC
Digital control I²C, SPI or other runtime configuration TPS65219-Q1 and STPMIC1L support I²C
Package / thermal path PCB area, exposed pad and heat transfer STPMIC1L: 4 × 4 × 1 mm VFQFPN-28

Protection features should also match the application. Useful functions can include:

  • Overcurrent protection (OCP)
  • Overvoltage protection (OVP)
  • Undervoltage lockout (UVLO)
  • Thermal shutdown
  • Short-circuit protection
  • Soft start
  • Output discharge
  • Power-good and fault reporting

Finally, do not select a PMIC from electrical specifications alone. Package size, exposed thermal pad, junction temperature, PCB copper area, thermal vias, external inductors and capacitors all affect how much usable power the PMIC can deliver in the finished board.

Where Are PMICs Used?

PMICs are common wherever electronic systems require several controlled voltage domains in limited PCB space.

Typical applications include:

  • Smartphones
  • Tablets
  • Wearables
  • IoT devices
  • Edge AI hardware
  • Embedded Linux systems
  • FPGA boards
  • Automotive infotainment
  • ADAS electronics
  • Industrial control systems
  • Medical devices
  • Networking equipment
  • Cameras and imaging systems

A smartphone PMIC may manage the processor, memory, display, camera, radio, battery, and always-on rails.

An FPGA or edge-computing board may use a PMIC to supply core, auxiliary, I/O, memory, and transceiver voltages in a defined sequence.

Automotive PMICs may add watchdogs, safety monitoring, protected outputs, and communication with the main processor. The underlying architecture changes by application, but the common requirement is coordinated management of several power domains.

What PCB Layout Rules Matter for a PMIC?

PMIC PCB layout is critical because switching converters combine high current, fast switching edges, sensitive feedback nodes, and thermal dissipation within a small area.

Important layout rules include:

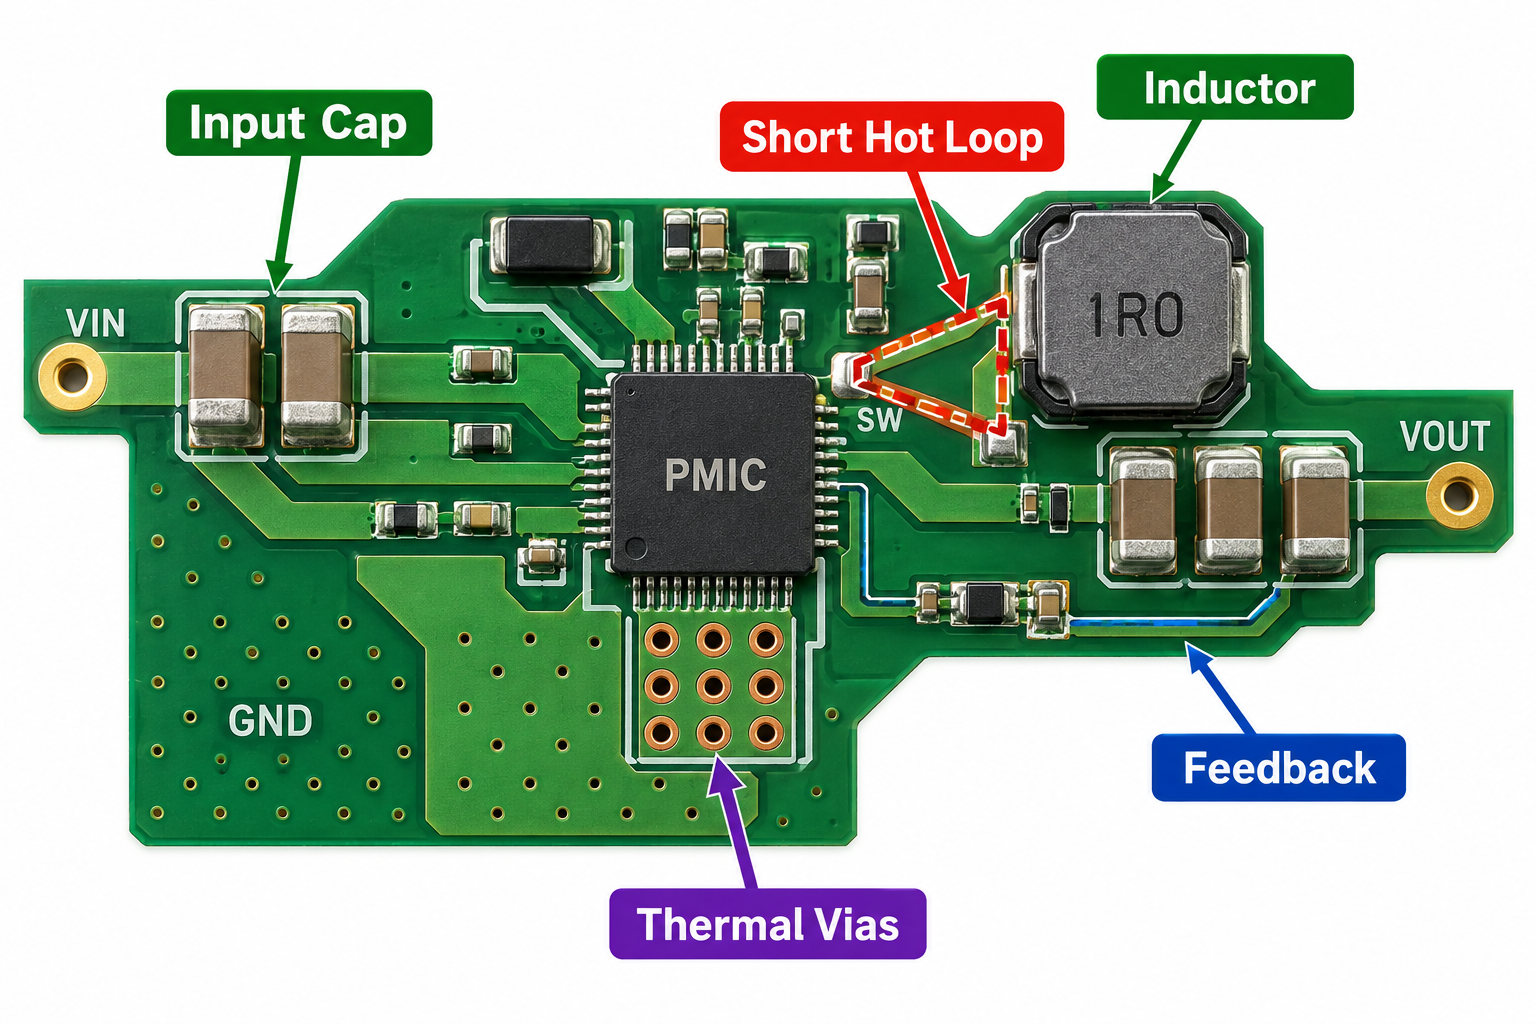
  • Place input capacitors close to VIN and power ground.
  • Minimize high-di/dt switching loops.
  • Keep inductors close to switching pins.
  • Keep the SW node compact.
  • Route feedback away from noisy switching nodes.
  • Use wide copper for high-current paths.
  • Provide low-impedance ground return paths.
  • Place output capacitors close to their rails.
  • Use thermal vias under exposed pads where required.
  • Avoid routing sensitive analog signals through switching-current paths.

The input capacitor, switching FETs, inductor, and output capacitor form critical current loops. Increasing their loop area raises parasitic inductance and can worsen ringing, EMI, and voltage ripple.

Grounding also needs to follow the PMIC vendor’s recommended layout. Analog ground, power ground, thermal pad connections, and feedback return paths should not be rearranged casually because the schematic appears electrically equivalent.

EBest Circuit can review PMIC placement, high-current copper, thermal vias, power planes, component spacing, and assembly requirements during PCB DFM.

PMIC PCB layout with input capacitor short hot loop inductor feedback routing and thermal vias

What Common PMIC Design Mistakes Cause Power Problems?

PMIC problems often come from system integration rather than a defective IC.

Common mistakes include:

  • Selecting a rail with insufficient output current
  • Ignoring processor startup or transient current
  • Using the wrong startup sequence
  • Incorrect power-down timing
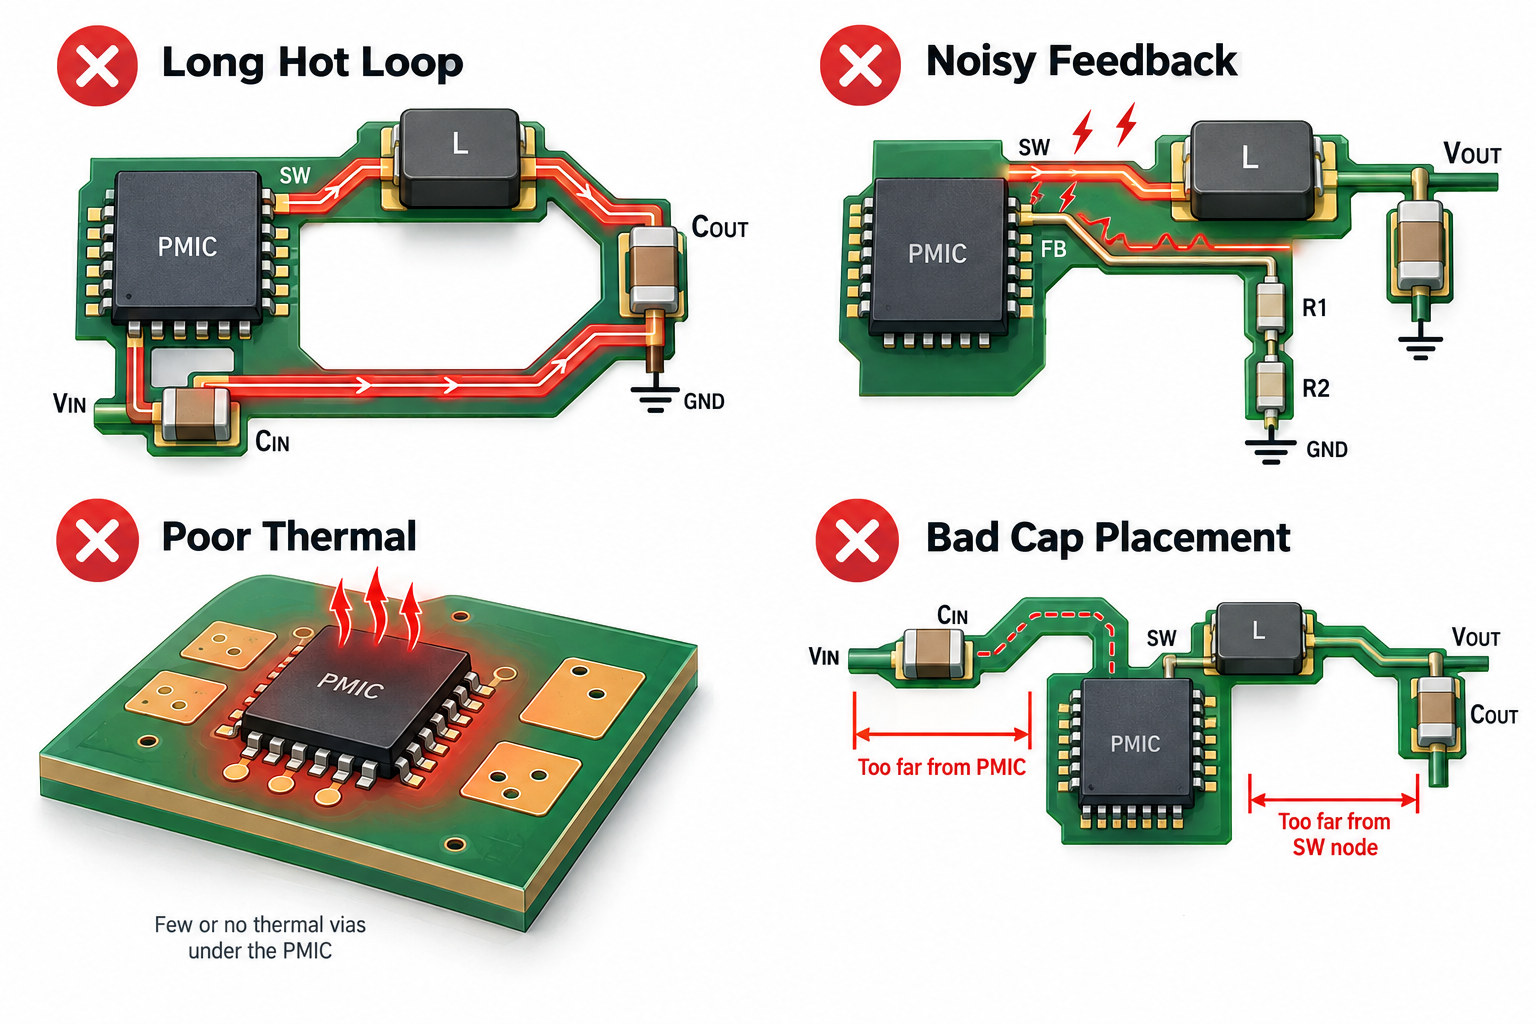
  • Poor input or output capacitor placement
  • Choosing the wrong inductor
  • Routing feedback close to the SW node
  • Making switching hot loops too large
  • Inadequate thermal vias
  • Excessive copper loss on high-current rails
  • Ignoring PMIC configuration or OTP settings
  • Using the wrong I²C address
  • Forgetting power-good or reset timing requirements
  • Assuming every rail can run at maximum current simultaneously

Thermal design is another frequent issue. A PMIC supplying several rails can dissipate significant heat even when individual converters operate efficiently.

The exposed thermal pad, PCB copper area, via array, airflow, ambient temperature, and neighboring heat sources all affect junction temperature.

Startup testing should therefore be performed with the real processor, memory, and peripherals rather than only checking the PMIC outputs with no load.

Common PMIC PCB design mistakes including long hot loop noisy feedback poor thermal design and bad capacitor placement

How Should a PMIC Design Be Prepared for PCB Assembly and Testing?

PMIC assembly requirements depend strongly on the package. QFN, BGA, and WLCSP devices need different stencil, placement, inspection, and rework strategies.

For QFN PMICs, review:

  • Exposed thermal pad
  • Paste aperture ratio
  • Thermal via layout
  • Solder-mask definition
  • Void control
  • Package orientation

For BGA or WLCSP packages, additional concerns include:

  • Fine-pitch pad geometry
  • Via-in-pad requirements
  • Solder-mask registration
  • Board warpage
  • X-ray inspection
  • Rework capability

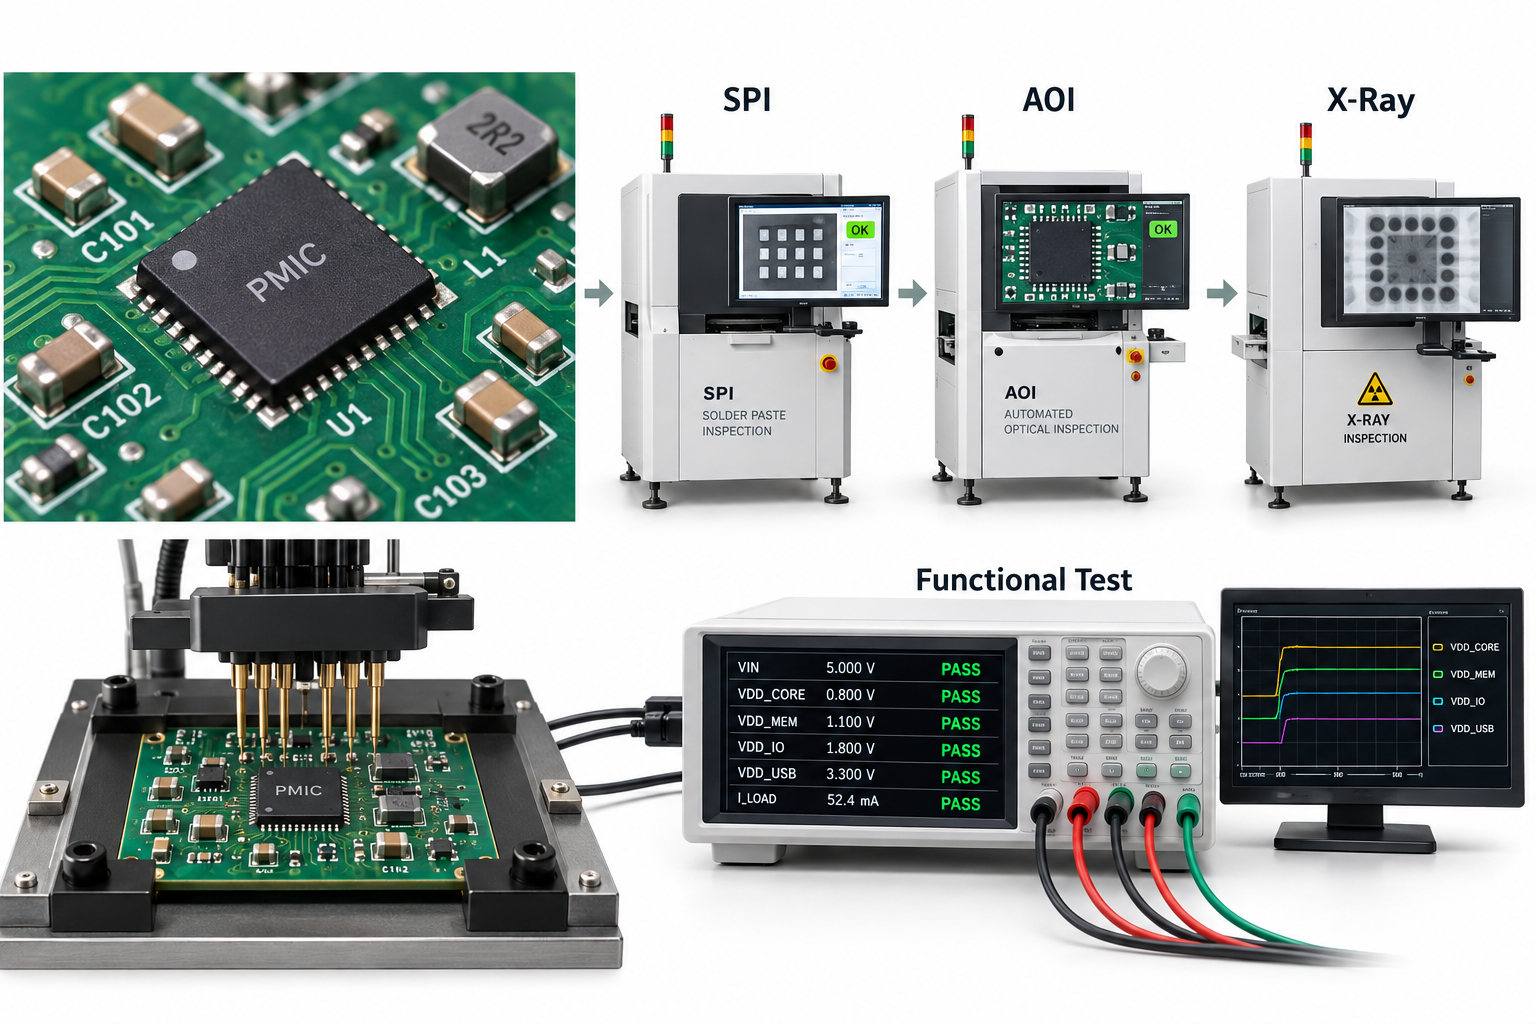
A production test plan should verify more than static output voltage. Useful checks can include:

  • Rail startup sequence
  • Rail shutdown sequence
  • Output-voltage accuracy
  • Ripple
  • Load response
  • Power-good timing
  • Reset timing
  • Fault response
  • I²C/SPI communication
  • Thermal behavior under load

SPI can verify solder-paste deposition before placement, while AOI helps inspect visible joints and nearby passives. X-ray is particularly useful for hidden BGA/WLCSP joints and exposed-pad voiding where relevant.

PMIC PCB assembly and testing flow with SPI AOI X-ray and functional test equipment

FAQ About PMIC Power Management ICs

1. What does PMIC stand for?
The PMIC full form is Power Management Integrated Circuit.

2. What is PMIC in electronics?
The PMIC meaning in electronics is a chip that generates, regulates, sequences, monitors, and protects one or more system power rails.

3. Is a PMIC chip the same as a voltage regulator?
No. A voltage regulator normally controls one rail, while a PMIC chip can integrate several regulators plus sequencing, monitoring, protection, charging, or digital control.

4. Does a PMIC need external components?
Usually yes. Depending on the architecture, a PMIC may require external inductors, input and output capacitors, resistors, sense components, and sometimes external MOSFETs.

5. Why is power sequencing important in a PMIC?
Processors, memory, and I/O rails may need to start and stop in a defined order. Incorrect sequencing can cause startup failure, excessive current, or undefined system behavior.

6. Can one PMIC power a processor, memory and peripherals?
Yes, if the PMIC provides the required number of rails, voltage ranges, output currents, sequencing, and total thermal capacity.

Planning a PCB Around a PMIC?

A PMIC can simplify a complex power tree, but its performance still depends on the surrounding PCB. High-current loops, inductors, decoupling, feedback routing, thermal pads, sequencing signals, and assembly quality all need to be considered together.

EBest Circuit supports PMIC-based PCB fabrication, DFM review, fine-pitch SMT assembly, component sourcing, SPI, AOI, X-ray inspection, and functional testing. For a new power-management PCB project, send your Gerber files, BOM, schematic, stackup, and power requirements to sales@bestpcbs.com for engineering review.

You may also like

TQFP Package: Dimensions, Pin Counts, LQFP/QFN Comparison & PCB Guide

September 17th, 2026

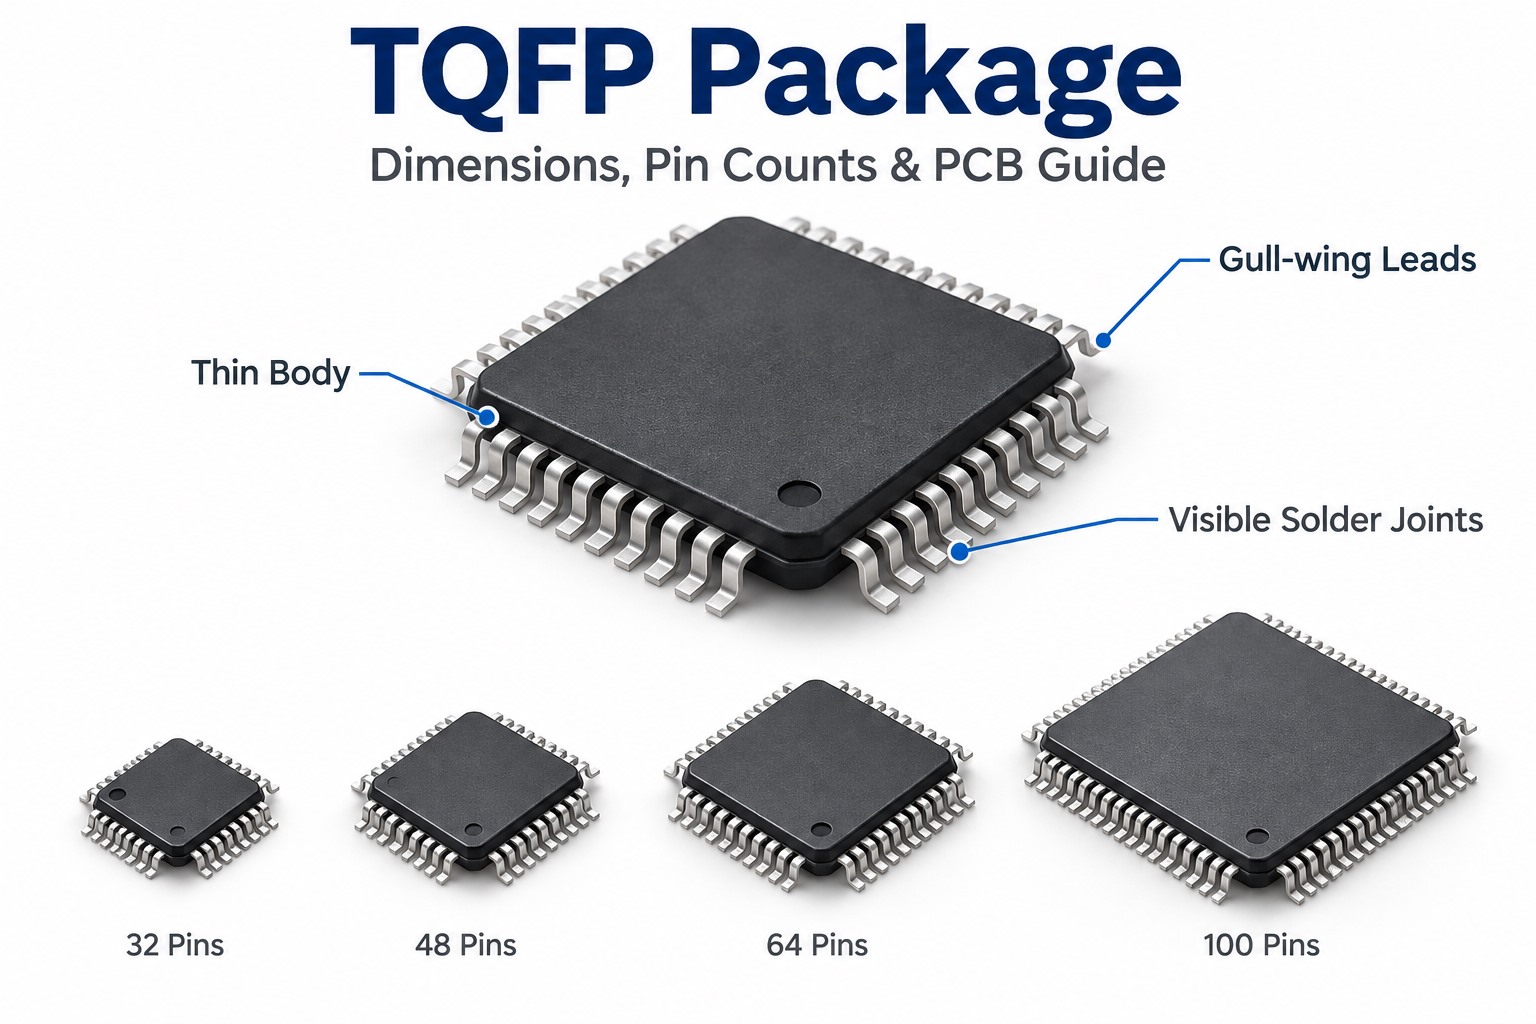
The TQFP package remains widely used for microcontrollers, mixed-signal ICs, communication devices, motor-control ICs, and other components that need moderate to high I/O counts without moving to BGA packaging. Their exposed gull-wing leads also make them attractive when visual solder inspection, prototyping, and rework matter.

The main challenge is that “TQFP64” or “TQFP100” does not uniquely define a package. Two ICs can have the same TQFP pin count but different body sizes, lead pitches, or overall dimensions. For PCB designers, the correct workflow is therefore part number → package drawing → land pattern, not pin count → generic footprint.

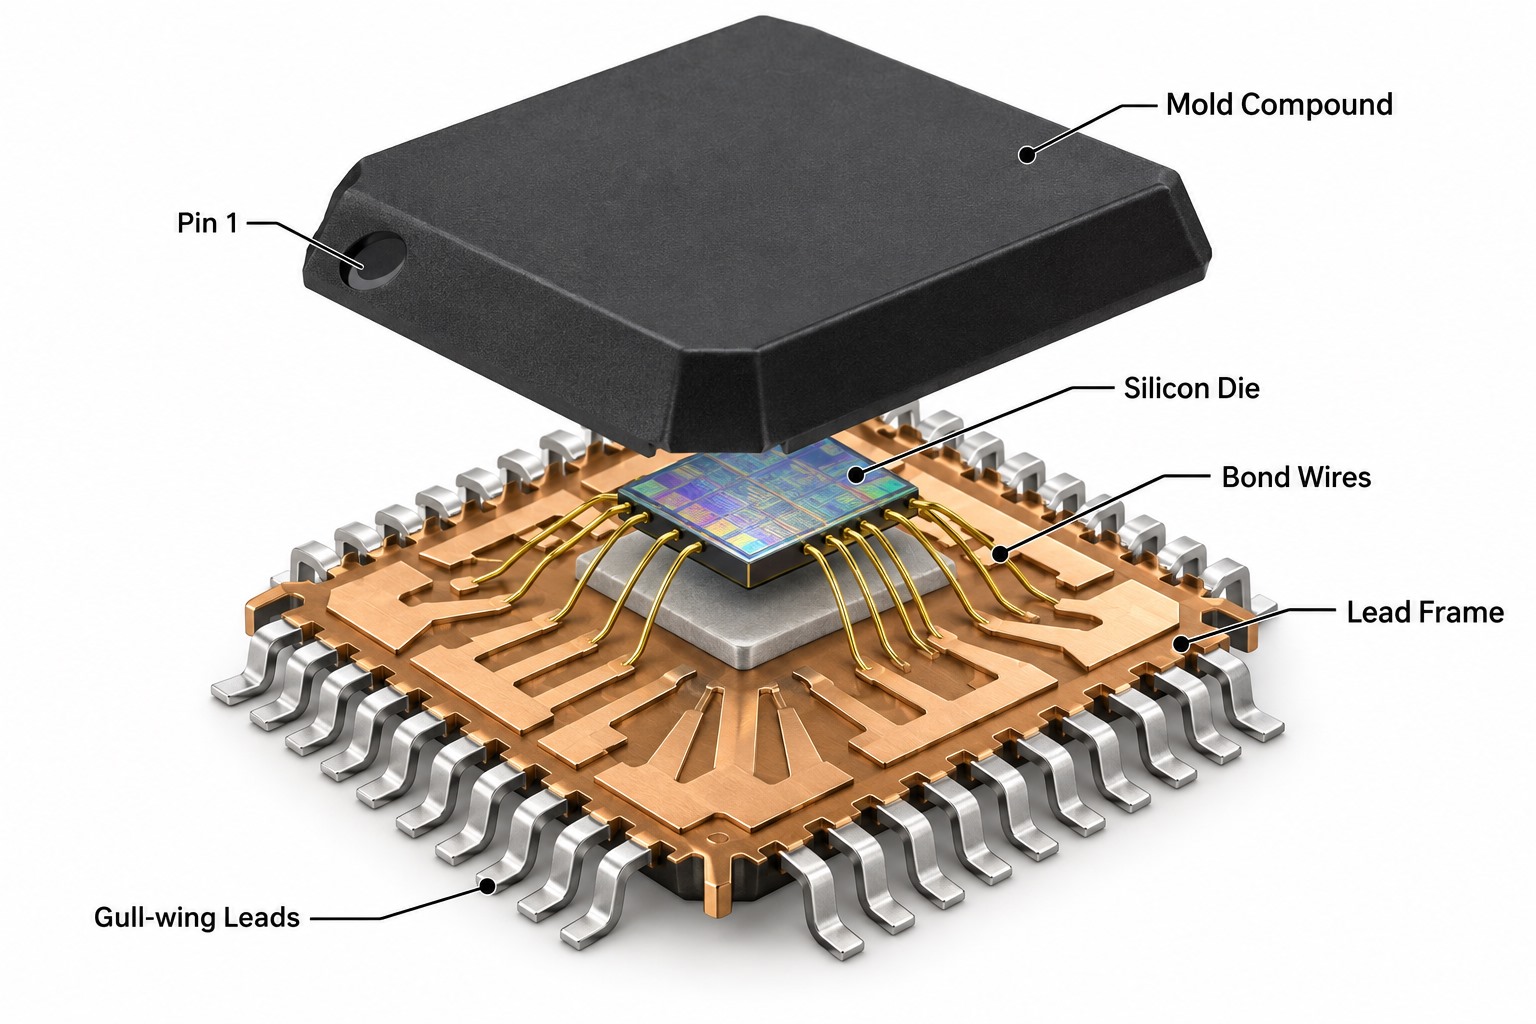
TQFP package overview showing thin body gull-wing leads visible solder joints and common pin counts

Key Takeaways

  • TQFP stands for Thin Quad Flat Package, a surface-mount IC package with gull-wing leads extending from all four sides.
  • TQFP is a package family, not one fixed footprint. Pin count alone does not determine body size, lead pitch, or PCB land pattern.
  • Common examples include TQFP32, TQFP44, TQFP48, TQFP64, TQFP100, and TQFP144, but dimensions can vary between semiconductor manufacturers.
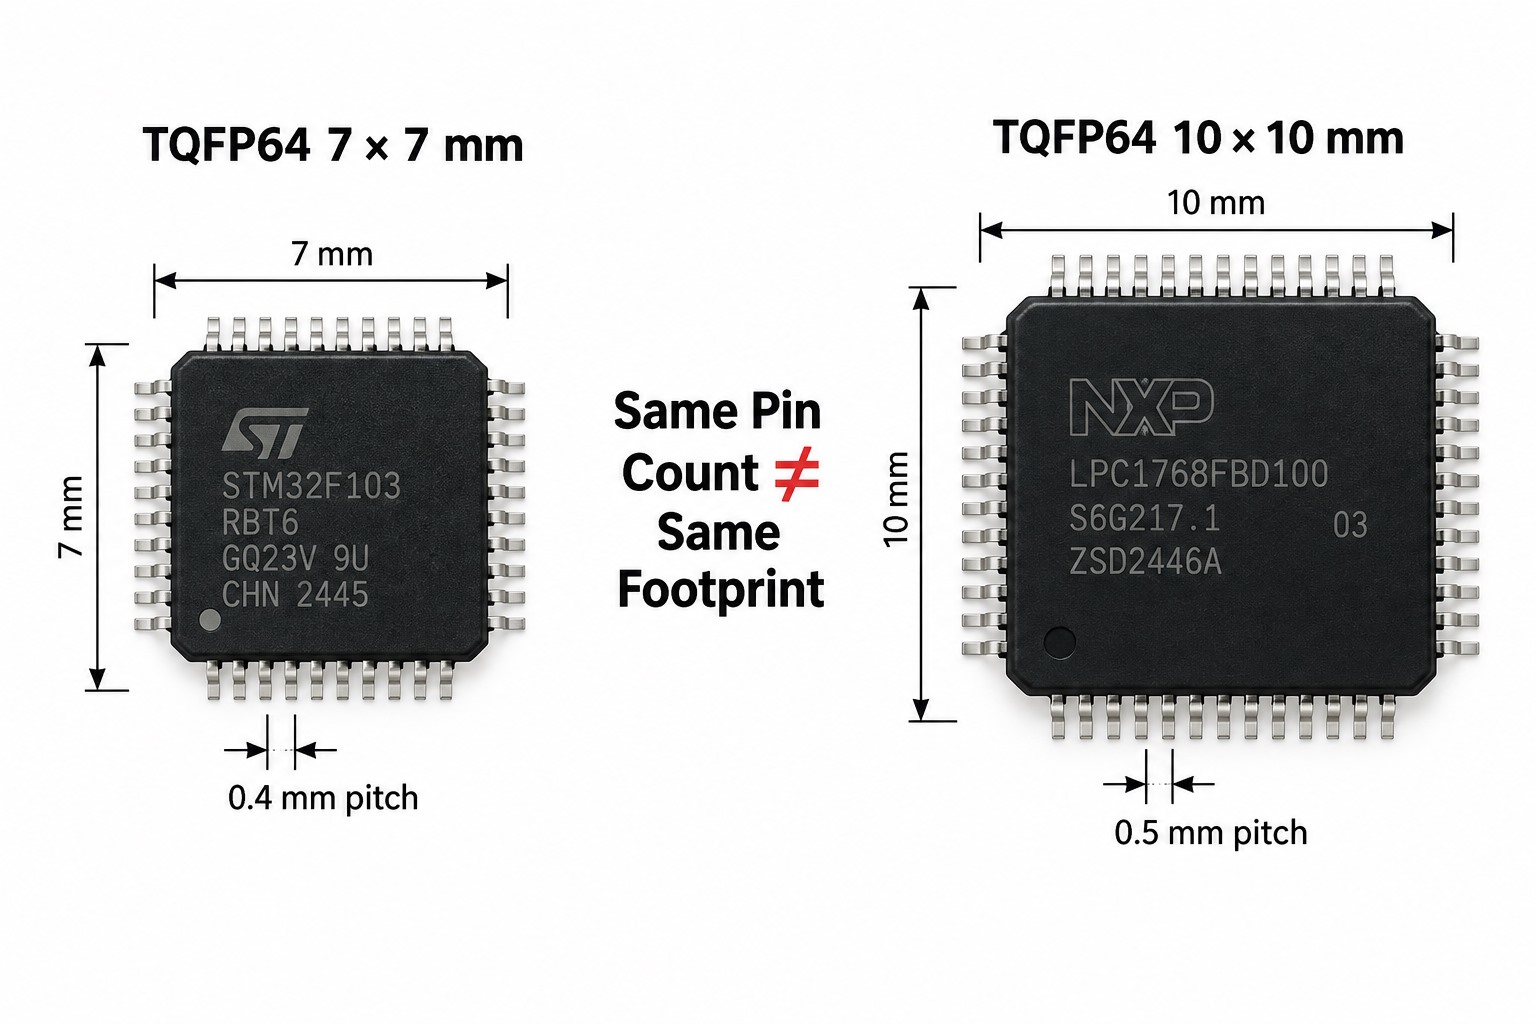
  • For example, NXP lists both 10 × 10 mm and 7 × 7 mm TQFP64 packages, showing why “TQFP64” is not enough information for footprint selection.
  • TQFP and LQFP are closely related QFP variants, but package names alone do not guarantee footprint compatibility.
  • Compared with QFN, TQFP uses visible gull-wing leads, which makes solder-joint inspection and rework easier but requires more PCB area.
  • PCB footprints should always be built from the exact manufacturer package drawing, including pitch, body size, overall lead span, lead width, lead length, and package orientation.

What Is a TQFP Package?

TQFP stands for Thin Quad Flat Package, it is a surface-mount package with leads extending from all four sides of a thin molded body. It belongs to the broader QFP, or Quad Flat Package, family. The leads are formed into a gull-wing shape so they can sit on PCB pads and be soldered by standard SMT reflow processes.

Typical TQFP characteristics include:

  • Leads on four sides
  • Gull-wing lead shape
  • Surface-mount assembly
  • Relatively low package profile
  • Fine lead pitch
  • Visible solder joints
  • Pin counts from a few dozen to well above 100

A TQFP package is commonly used when the IC needs more I/O than SOIC or similar two-sided packages can provide but the design does not require BGA-level interconnect density.

How Is a TQFP Package Constructed?

A TQFP package normally contains a silicon die mounted inside a molded plastic body and electrically connected to an external lead frame.

Its basic construction includes:

  • Silicon die
  • Die attach material
  • Bond wires or equivalent internal interconnection
  • Copper-alloy lead frame
  • Mold compound
  • Gull-wing leads
  • Pin 1 orientation mark

The lead frame carries signals from the silicon die to the external terminals. After molding, the leads extend outward from all four sides and bend downward toward the PCB.

The package body itself is smaller than the total installed footprint because the leads extend beyond the molded body. This distinction matters during placement and land-pattern design.

Exploded TQFP package construction showing mold compound silicon die bond wires lead frame gull-wing leads and pin 1

What Dimensions Define a TQFP Package?

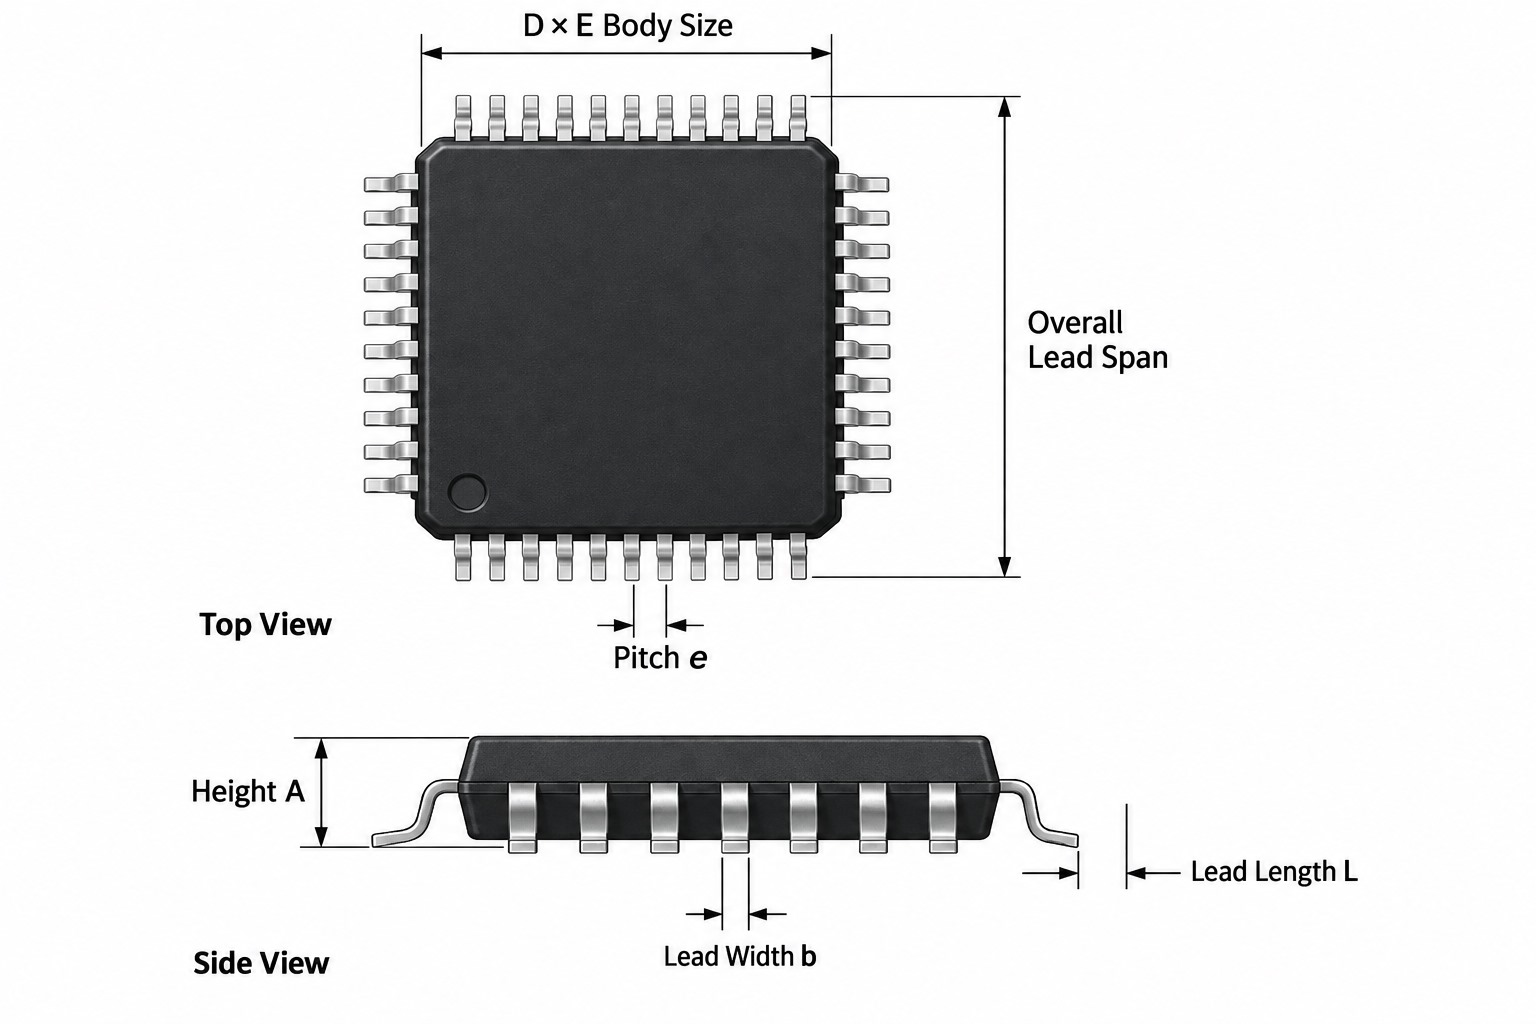
TQFP package dimensions include several mechanical values, not just the molded body width.

Parameter What It Describes
D × E Molded body length and width
HD × HE or overall D × E Total span including leads
A Overall package height
A1 Standoff above the PCB seating plane
e Lead pitch
b Lead width
L Gull-wing lead length
N Total lead count

Body size and overall lead span are not the same dimension. A PCB footprint designed only from the stated body size can miss the additional space occupied by the gull-wing leads.

TQFP package dimension drawing showing body size overall lead span pitch height lead width and lead length

TQFP32, 44, 48, 64, 100 and 144: What Are the Common Dimensions?

TQFP packages appear in many pin counts, but the following values should be treated as representative package examples rather than universal dimensions.

Package Example Representative Body Size Representative Pitch
TQFP32 7 × 7 mm 0.80 mm
TQFP44 10 × 10 mm 0.80 mm
TQFP48 7 × 7 mm 0.50 mm
TQFP64 7 × 7 or 10 × 10 mm examples 0.40 or 0.50 mm examples
TQFP100 14 × 14 mm 0.50 mm
TQFP144 16 × 16 mm example 0.40 mm

The package name should therefore never replace the exact IC mechanical drawing.

Representative TQFP32 TQFP44 TQFP48 TQFP64 TQFP100 and TQFP144 package examples

Does the Same TQFP Pin Count Always Mean the Same Footprint?

No. The same TQFP pin count does not guarantee the same body size, lead pitch, lead span, or PCB footprint.

TQFP64 is a clear example. Different vendors offer 64-pin packages in multiple body sizes and pitches, so a CAD library entry named only “TQFP64” is not sufficiently specific for production.

Before reusing a footprint, compare:

  • Body dimensions
  • Overall lead span
  • Lead pitch
  • Lead width
  • Lead length
  • Package height
  • Pin 1 orientation

A footprint can look plausible on screen and still be completely incompatible with the physical component.

TQFP64 comparison showing same 64 pin count with 7 by 7 mm and 10 by 10 mm packages and different pitch

TQFP vs QFP: What Is the Difference?

QFP is the broader Quad Flat Package family, while TQFP is a thinner-profile member of that family.

Both use:

  • Leads on four sides
  • Gull-wing terminals
  • Surface-mount assembly
  • Similar general soldering methods

The difference is mainly in the mechanical outline and package profile. TQFP should therefore not be treated as a package technology completely separate from QFP; it is better understood as a thinner mechanical implementation within the same four-sided leaded package concept.

TQFP vs LQFP: What Is the Difference?

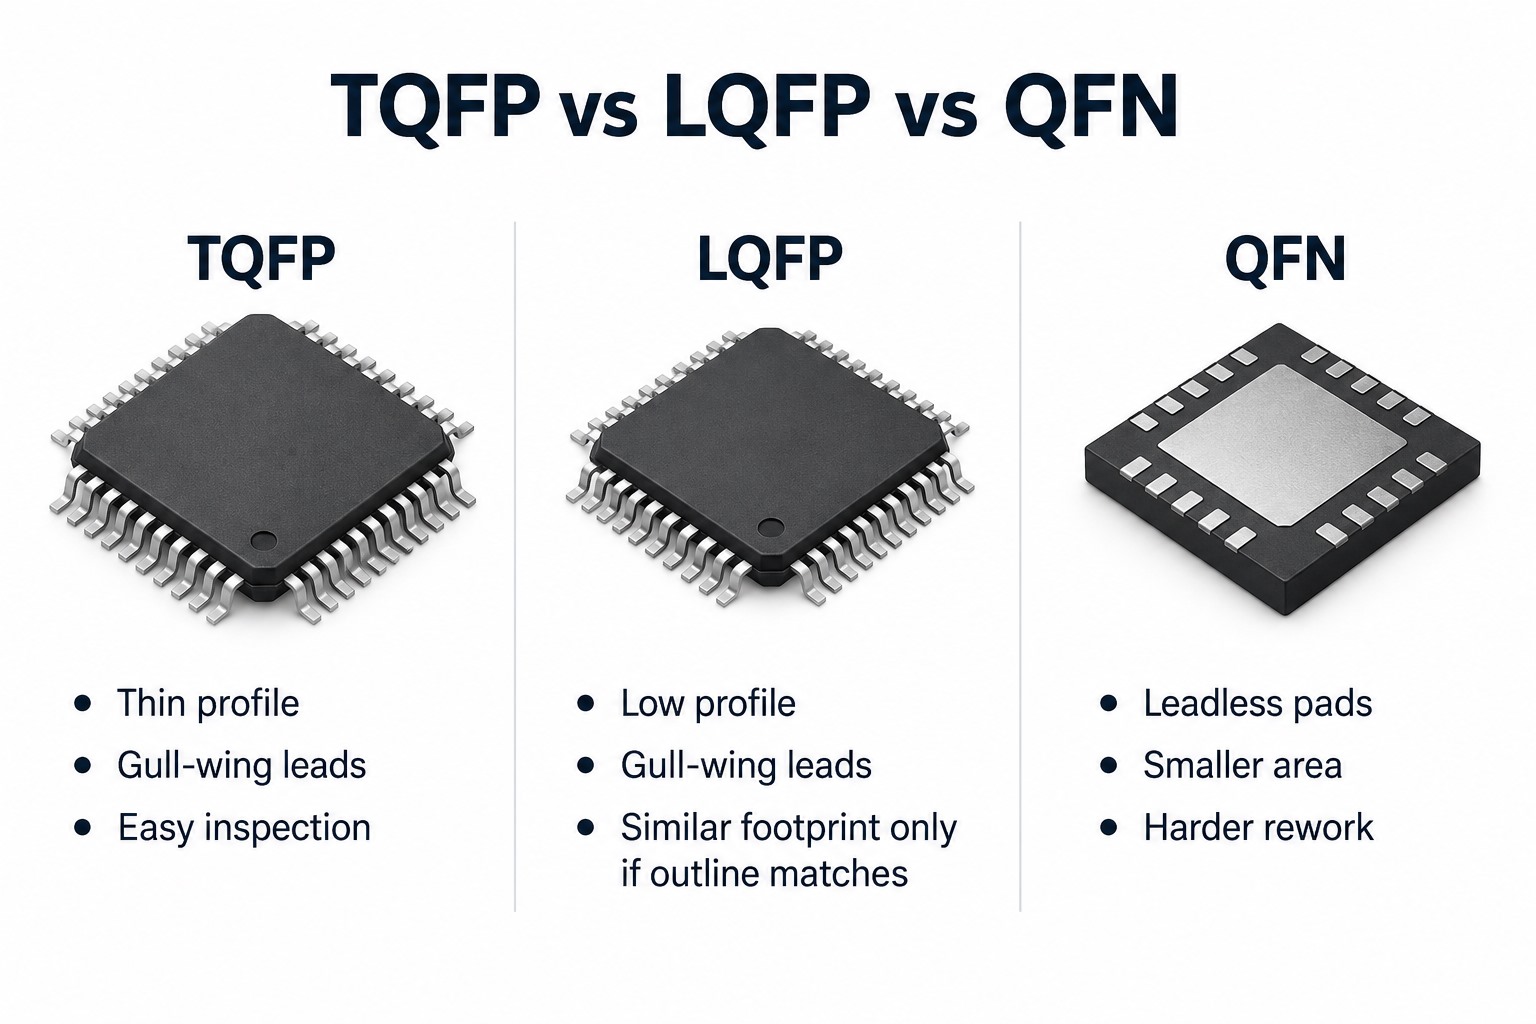
In a TQFP vs LQFP package comparison, both are closely related low-profile QFP variants. Their naming conventions can overlap enough that engineers should compare actual mechanical drawings instead of relying on the acronym.

Feature TQFP LQFP
Full name Thin Quad Flat Package Low-Profile Quad Flat Package
Leads Gull-wing Gull-wing
Mounting SMT SMT
Typical profile Thin Low profile
Common pitch range 0.4–0.8 mm 0.4–0.8 mm
Footprint compatibility Only if full outline matches Same rule

Never assume that TQFP and LQFP are footprint-compatible just because the pin count is the same.

TQFP vs QFN: Which Is Easier for PCB Assembly?

In a TQFP vs QFN package comparison, TQFP is generally easier to inspect and rework because its gull-wing leads and solder joints are visible around the package perimeter.

Assembly Factor TQFP QFN
External leads Gull-wing Leadless bottom pads
Solder-joint visibility High Limited
AOI access Good Bottom joints less visible
X-ray requirement Usually not essential Often useful
Manual rework Easier More difficult
PCB area Larger Smaller
Fine-pitch defect risk Bridging / opens Insufficient wetting / voids
Thermal pad Package dependent Common on many QFNs

QFN can save significant PCB area and often offers a shorter electrical and thermal path, while TQFP remains attractive when inspection access and rework matter.

TQFP versus LQFP versus QFN package comparison

How Should a TQFP PCB Footprint Be Designed?

A TQFP PCB footprint should be created from the exact semiconductor manufacturer’s land-pattern or package drawing, not from a generic pin-count template.

Check these dimensions first:

  • Lead pitch
  • Lead width
  • Lead length
  • Molded body size
  • Overall lead span
  • Pin 1 orientation
  • Seating-plane information
  • Package tolerances

The PCB land pattern must also provide suitable solder fillets around the gull-wing leads. Toe, heel, and side fillets depend on the package geometry and the chosen land-pattern standard.

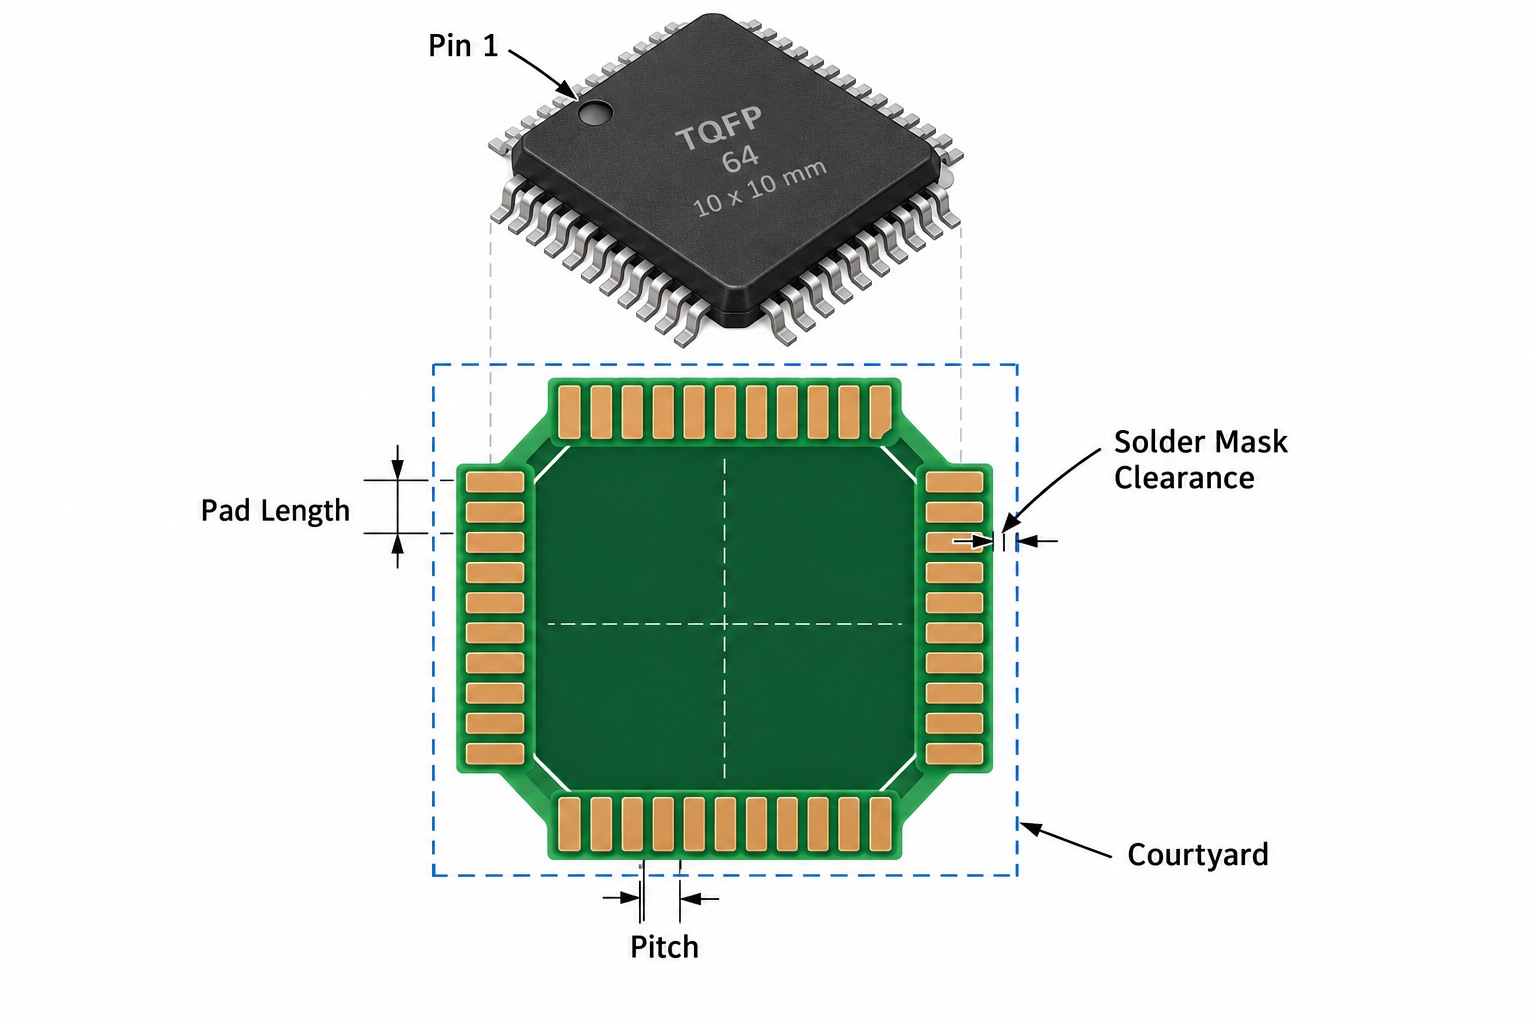
Also include clear pin 1 marking, solder-mask clearance, silkscreen that does not overlap pads, component courtyard, pick-and-place origin, and adequate neighboring-component clearance.

TQFP PCB footprint design showing pad length pitch solder mask clearance courtyard and pin 1

What SMT Assembly Problems Are Common with TQFP Packages?

The most common TQFP assembly defects involve fine-pitch leads, solder-paste volume, placement accuracy, and lead coplanarity.

Typical issues include:

  • Solder bridging
  • Insufficient solder
  • Open joints
  • Bent leads
  • Lifted leads
  • Lead coplanarity problems
  • Component misalignment
  • Wrong orientation
  • Contamination around fine-pitch pads

Solder bridging is especially common when pad geometry, stencil aperture, paste volume, or placement is poorly controlled. Fine-pitch packages leave little margin between adjacent solder deposits.

A robust SMT process may use solder paste inspection, accurate placement, controlled reflow, AOI, microscope inspection, and X-ray when hidden structures also require it.

Common TQFP SMT assembly defects including solder bridge open joint bent lead and misalignment

When Is TQFP a Good Package Choice?

TQFP is a practical choice when the design needs a moderate or high pin count while keeping solder joints visible and accessible.

It works particularly well for:

  • Microcontrollers
  • Industrial control ICs
  • Motor-control devices
  • Mixed-signal ICs
  • Communication controllers
  • Prototype and low-to-medium-volume assemblies
  • Products where rework access matters

TQFP may be less attractive when the design requires extremely high I/O density, minimum PCB area, very short high-speed interconnects, exceptional thermal dissipation, or package sizes smaller than exposed-lead QFP can provide.

For many industrial, automotive-control, instrumentation, and embedded applications, the additional board area is acceptable because the visible leads simplify inspection and troubleshooting.

FAQ About TQFP Packages

1. What does TQFP stand for?
TQFP stands for Thin Quad Flat Package. It is a surface-mount IC package with gull-wing leads on all four sides.

2. Is TQFP a surface-mount package?
Yes. TQFP is designed for surface-mount PCB assembly and is commonly soldered using SMT reflow.

3. What is the typical TQFP64 package size?
A common TQFP64 example is 10 × 10 mm with 0.5 mm pitch, but 7 × 7 mm TQFP64 packages also exist. Always check the exact IC datasheet.

4. What is the typical TQFP100 package size?
A common TQFP100 example is 14 × 14 mm with 0.5 mm lead pitch. Always verify the actual manufacturer drawing.

5. Is TQFP the same as LQFP?
No. They are closely related QFP variants, but the package profile and mechanical outline can differ. Some specific TQFP and LQFP parts may share a footprint only when all relevant dimensions match.

6. Can every TQFP with the same number of pins use the same PCB footprint?
No. Pin count alone does not define body size, pitch, lead span, or land pattern. A TQFP64, for example, can exist in multiple mechanical outlines.

If you are moving a TQFP-based design into fabrication or assembly, EBest Circuit can review the component package drawing, footprint, pad geometry, stencil requirements, orientation, BOM, and PCBA manufacturability before production. Send your Gerber files, BOM, placement files, and component datasheets to sales@bestpcbs.com for DFM review.
You may also like

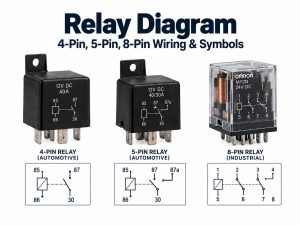
Relay Diagram: 4-Pin, 5-Pin, 8-Pin Wiring & Symbols Explained

September 17th, 2026

A relay diagram is easier to understand once you stop viewing the relay as one component and instead divide it into two sections. A low-power control circuit energizes the coil, while electrically separate contacts switch another circuit that may operate at a different voltage or carry much higher current.

This distinction explains most 4-pin, 5-pin, 8-pin, 14-pin, and 12V relay diagrams. The contact arrangement changes from one relay type to another, but the reading method stays similar: identify the coil, determine the contact form, confirm the pin numbering, and then check the actual device datasheet before wiring or PCB layout.

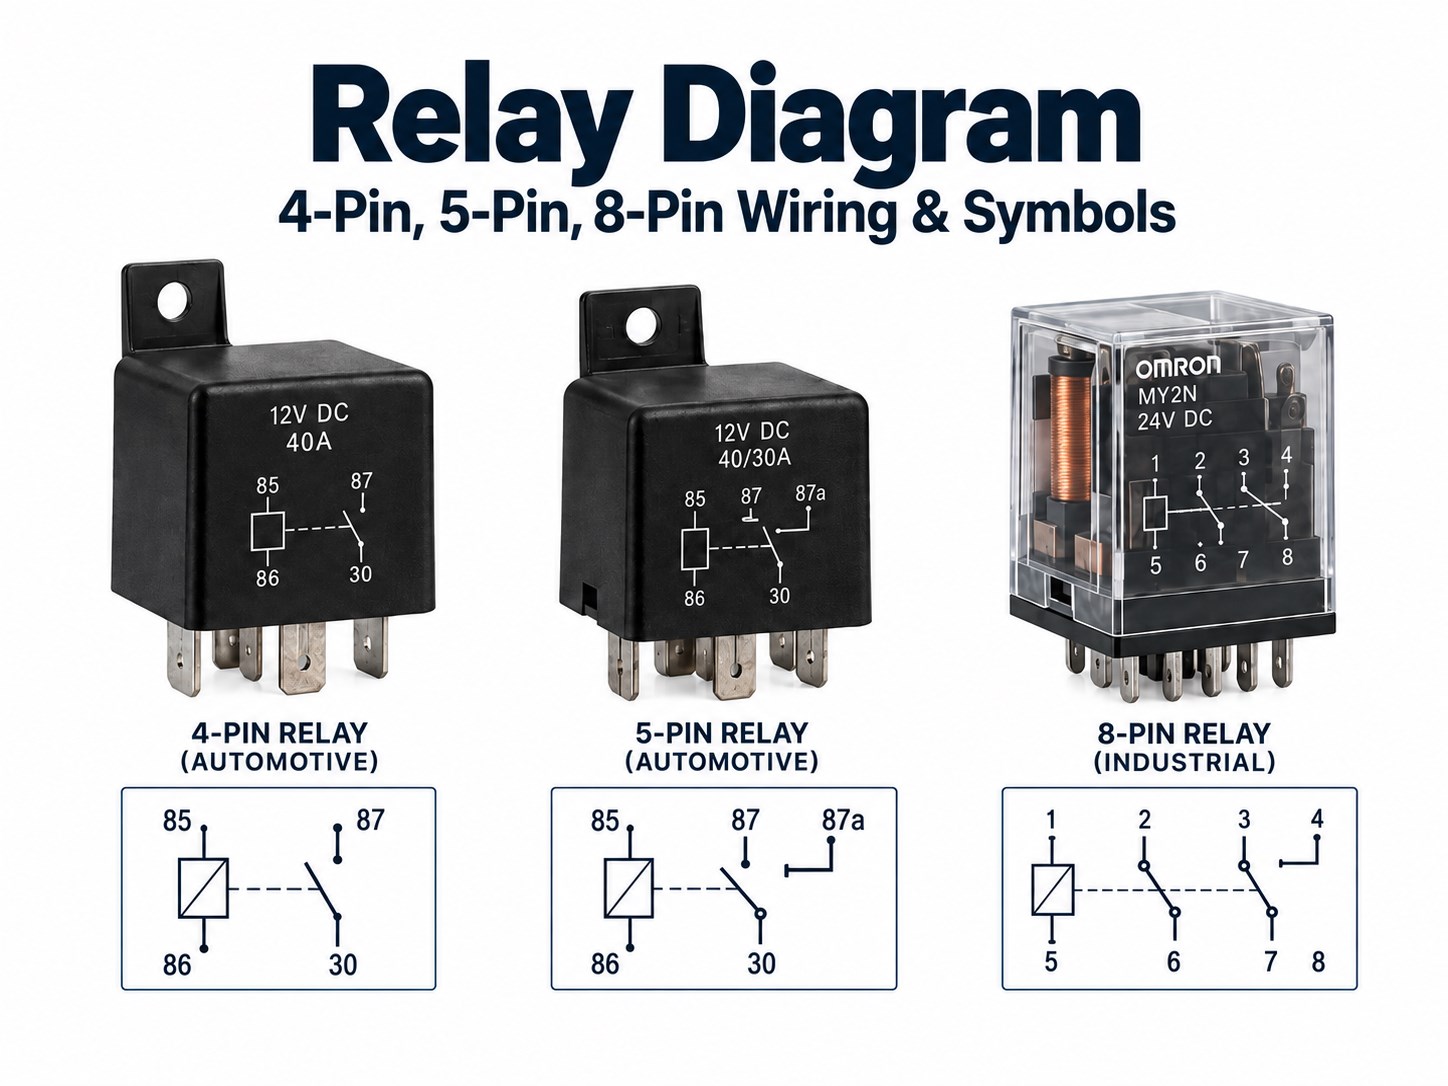
Relay diagram showing 4-pin 5-pin and 8-pin relay wiring and symbols

Key Takeaways

  • A relay diagram shows how the relay coil controls one or more electrical contacts and how those contacts connect or disconnect the load circuit.
  • The easiest way to read any relay is to separate it into a control side and a load side. The coil belongs to the control side; COM, NO, and NC belong to the switched side.
  • On common automotive relays, terminals 85 and 86 are typically the coil, 30 is common, 87 is normally open, and 87a is normally closed.
  • A common 4-pin automotive relay is usually SPST and normally open, while a common 5-pin version adds a normally closed contact and behaves as an SPDT relay.
  • An 8-pin relay is often DPDT, while many 14-pin relays provide four changeover contact sets. Physical pin numbering is not universal, so the datasheet must still be checked.
  • Relay schematic symbols, wiring diagrams, pin diagrams, and PCB footprints describe different things. A correct schematic can still produce a wrong PCB if the footprint orientation or pin mapping is mirrored.
  • Coil polarity may matter when a relay contains an internal diode, LED, or other polarity-sensitive suppression component.

What Is a Relay Diagram?

A relay diagram shows the relay coil, switching contacts, terminal functions, and the electrical relationship between the control circuit and the load circuit.

Several diagram types are commonly called a “relay diagram,” although they provide different information:

  • Schematic diagram: Shows electrical function.
  • Wiring diagram: Shows how wires connect between devices.
  • Pin diagram: Shows terminal or pin assignments.
  • Internal relay diagram: Shows the coil and contact arrangement inside the relay.
  • PCB footprint: Shows the actual pad or hole positions used for board layout.

A schematic may tell you that a relay is SPDT, but it does not necessarily tell you which physical pin is at the top-left corner of the package. That information comes from the relay pinout or package drawing.

This is why a relay diagram should always be matched to the exact relay model before wiring or creating a PCB footprint.

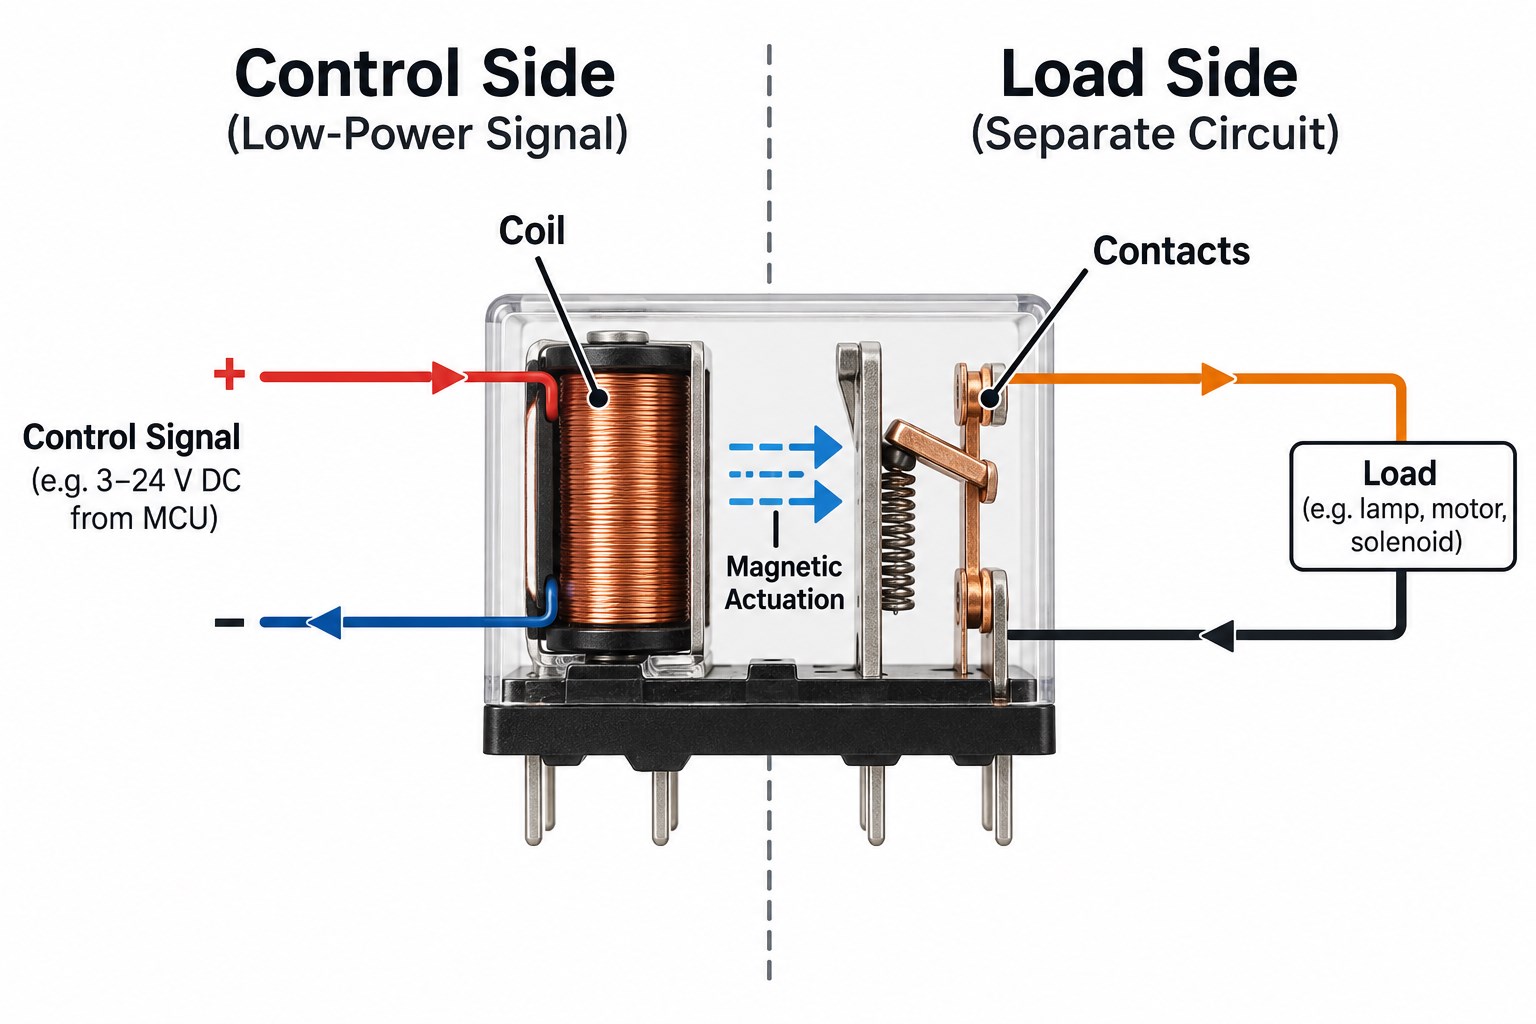
How Does a Relay Diagram Separate the Control Side from the Load Side?

A relay diagram normally separates the device into a control side containing the coil and a load side containing the contacts.

The relationship can be simplified as:

Control voltage → Coil → Magnetic force → Moving contact → Load circuit changes state

The coil is electrically isolated from the switched contacts in a conventional electromechanical relay. Applying the rated coil voltage creates a magnetic field that moves an armature and changes the contact position.

For example, a 12V control signal may energize a relay coil while the contacts switch a higher-current lamp, motor, pump, heater, or another circuit.

Relay control side and load side showing coil magnetic actuation and isolated contacts

What Do Coil, COM, NO and NC Mean on a Relay Diagram?

Coil, COM, NO, and NC describe the main functional parts found in common electromechanical relay diagrams.

Marking Meaning Coil De-Energized
Coil Electromagnetic control input No magnetic actuation
COM Common moving contact Connected according to normal state
NO Normally Open Open
NC Normally Closed Connected to COM

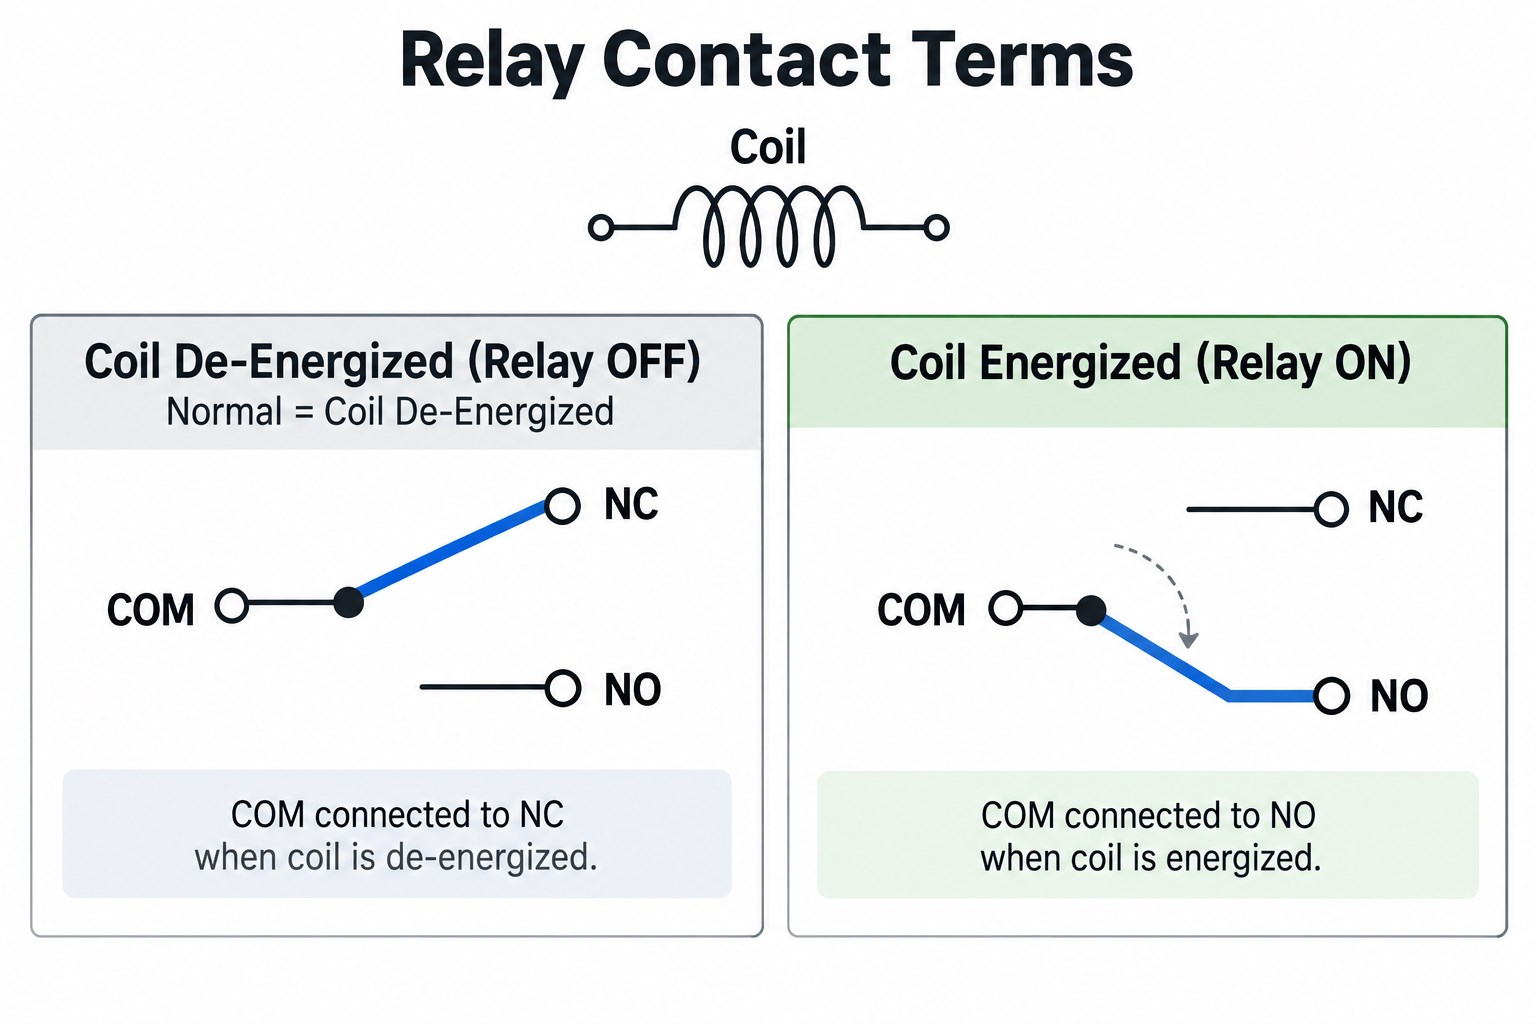
The word “normally” means the relay coil is not energized. It does not describe the state during normal machine operation.

In an SPDT relay, COM connects to NC when the coil is off. When the coil is energized, the contact moves away from NC and connects COM to NO.

Relay contact terms showing COM NO and NC when coil is de-energized and energized

Relay Diagram Symbols: How Do You Read the Coil and Contacts?

Relay symbols show the electrical relationship between the coil and the contacts rather than the physical appearance of the relay.

A schematic typically includes:

  • A coil symbol
  • One or more contact symbols
  • NO or NC contact positions
  • A dashed mechanical relationship between the coil and contacts
  • A device designator such as K1, K2, RY1, or REL1

A dashed line between the coil and contacts represents mechanical linkage, not an electrical wire. When multiple contact sets share the same relay designation, one coil operates all of those contacts together.

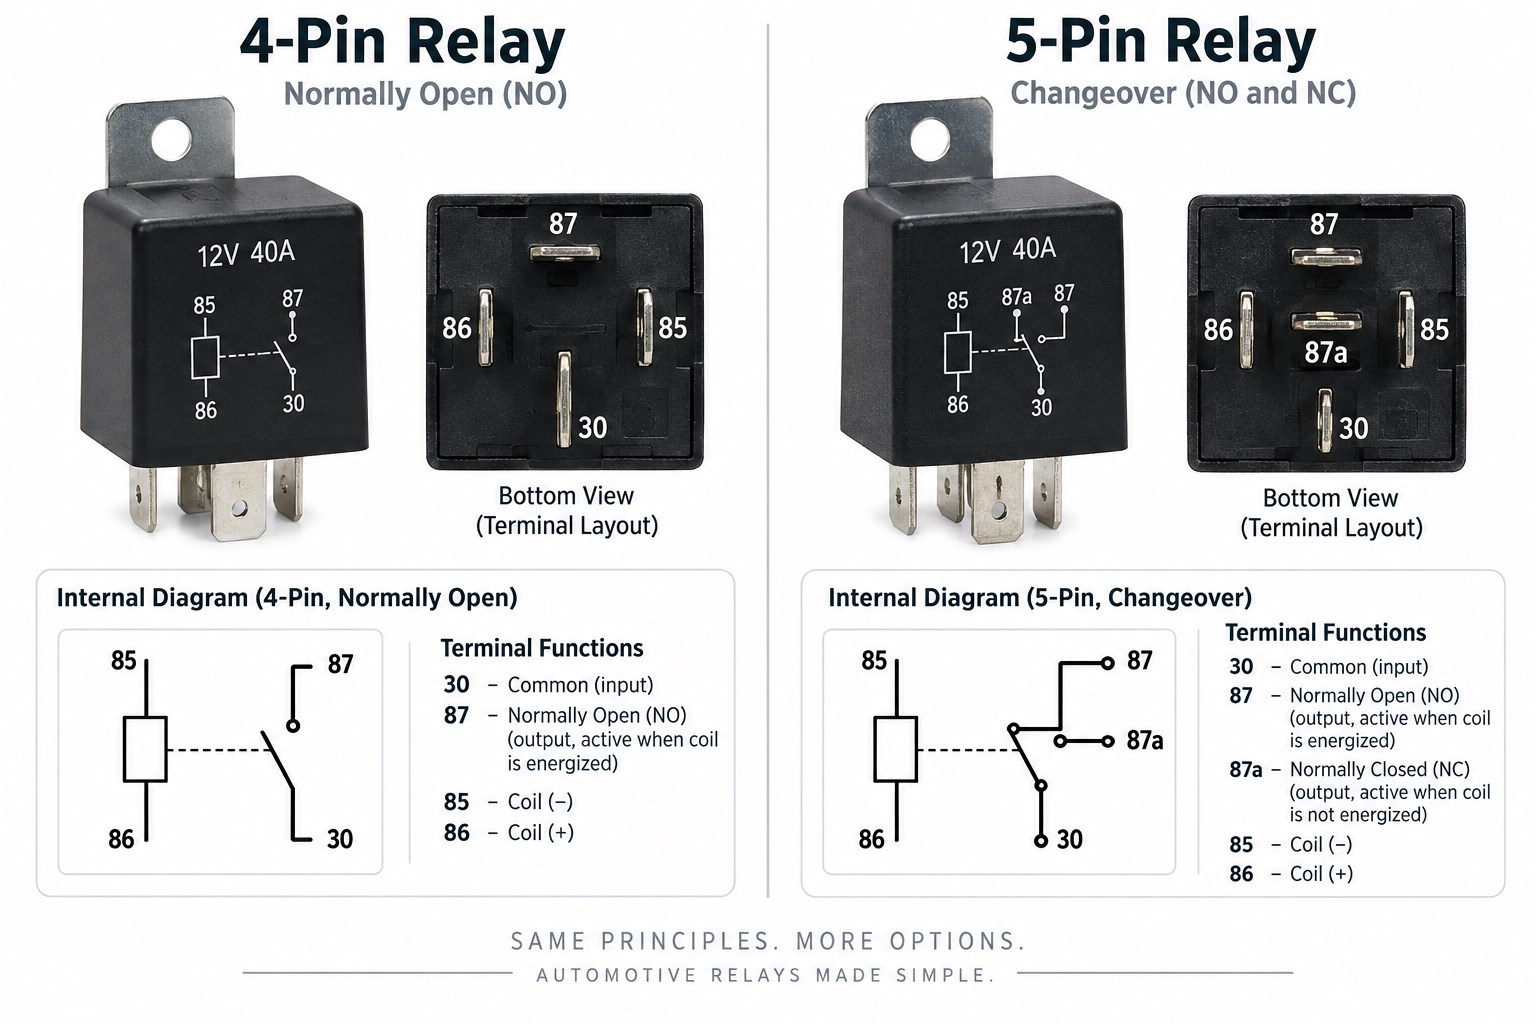
4-Pin vs 5-Pin Relay Diagram: What Do 30, 85, 86, 87 and 87a Mean?

A common automotive 4-pin relay uses terminals 30, 85, 86, and 87, while the common 5-pin changeover version adds terminal 87a.

A 4 pin relay diagram shows the coil and normally-open switching path. A 5 pin relay diagram adds the 87a normally-closed path.

Terminal Common Automotive Function
85 Coil
86 Coil
30 Common power contact
87 Normally open contact
87a Normally closed contact

A typical 4-pin automotive relay is an SPST normally-open relay. With the coil off, 30 and 87 are open; when voltage is applied across 85 and 86, terminal 30 connects to 87.

A common 5-pin relay adds terminal 87a and usually operates as an SPDT changeover relay. With the coil off, 30 connects to 87a; when energized, 30 transfers to 87.

4-pin and 5-pin automotive relay diagram showing terminals 30 85 86 87 and 87a

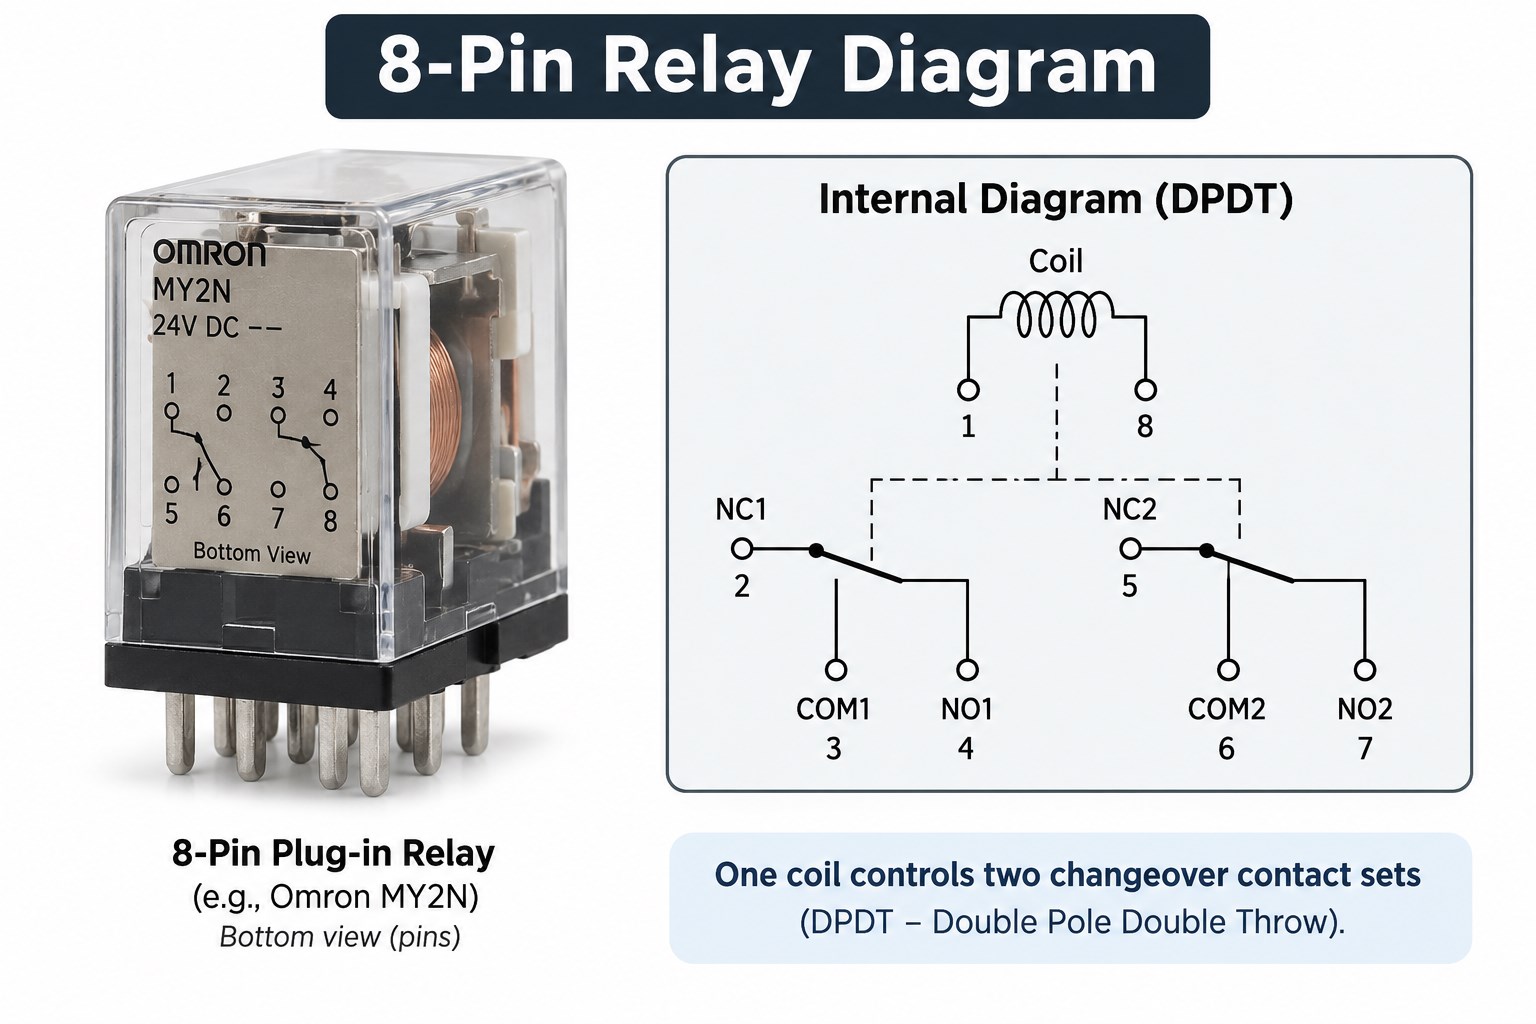
How Do You Read an 8-Pin Relay Diagram?

An 8-pin relay is commonly a DPDT relay containing one coil and two independent changeover contact sets. An 8 pin relay diagram therefore shows both contact sets operated by the same coil.

Its internal functions normally include:

  • 2 coil terminals
  • 2 COM terminals
  • 2 NO terminals
  • 2 NC terminals

That gives a total of eight pins. Conceptually, the relay contains two SPDT switches operated by the same coil.

There is no universal physical numbering arrangement for every 8-pin relay. The relay case diagram and datasheet should therefore be checked before connecting an 8-pin socket or creating a PCB footprint.

8-pin DPDT relay diagram with two changeover contact sets

What Does a 14-Pin Relay Diagram Usually Show?

A 14-pin relay often provides four changeover contact sets operated by one coil, commonly described as 4PDT or 4CO.

A typical functional breakdown is:

  • 2 coil terminals
  • 4 COM terminals
  • 4 NO terminals
  • 4 NC terminals

That totals 14 electrical connections. These relays are common in industrial control panels, PLC interface circuits, interlocking systems, alarm circuits, machine control, and signal distribution.

As with 8-pin relays, the 14-pin count does not guarantee one universal physical pin sequence. Socket numbering and terminal arrangement must be verified against the exact part number.

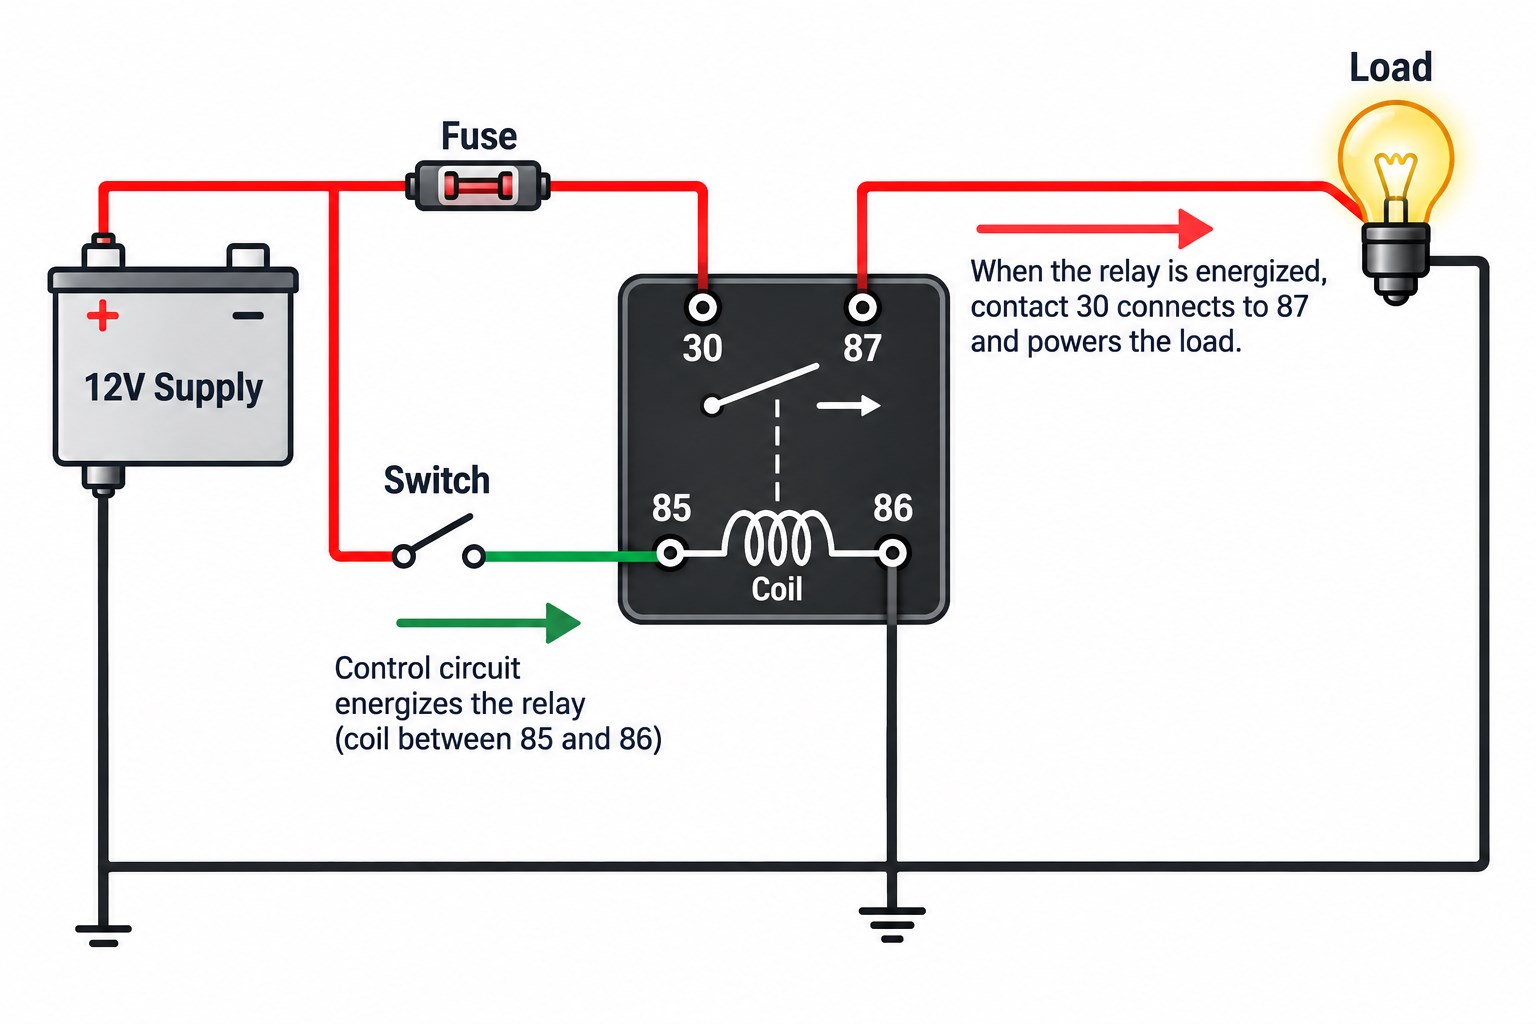
How Do You Read a 12V Relay Wiring Diagram?

A 12V relay wiring diagram should be read by checking the coil circuit first and then tracing the switched load circuit.

  1. Confirm the coil voltage. Make sure the relay is actually rated for a 12V coil.
  2. Identify the coil pins. These may be 85/86 on automotive relays or A1/A2 on industrial designs.
  3. Identify COM, NO, and NC. Determine which contact state the application needs.
  4. Check coil polarity. A plain coil may not be polarity-sensitive, but an internal diode or LED can make polarity mandatory.
  5. Protect the control device. Use appropriate coil suppression when required.
  6. Fuse the load circuit. The relay does not replace proper overcurrent protection.
  7. Check contact current and voltage ratings. Motor and lamp loads may have high startup current.
  8. Confirm wire size and grounding. The wiring must suit the actual load current.
12V 4-pin relay wiring diagram showing supply fuse switch coil terminals 85 86 and contacts 30 87

Where Are 4-Pin and 5-Pin Relay Diagrams Commonly Used?

Four-pin and five-pin automotive relay diagrams appear in many systems where a low-current control signal operates a higher-current electrical load.

Application Typical Relay Role
Horn Switch controls higher-current horn circuit
Starter Ignition/control path operates starter solenoid circuit
Fuel pump ECU or control circuit switches pump supply
Auxiliary light Dashboard switch controls lighting load
Cooling fan Sensor or ECU controls fan motor
Compressor Control circuit switches compressor clutch
Heater Low-current controller switches heating load

A horn relay, starter relay, fuel-pump relay, or driving-light relay still follows the same basic coil-and-contact logic. The application name does not define the internal relay pinout, so the actual relay markings must still be checked.

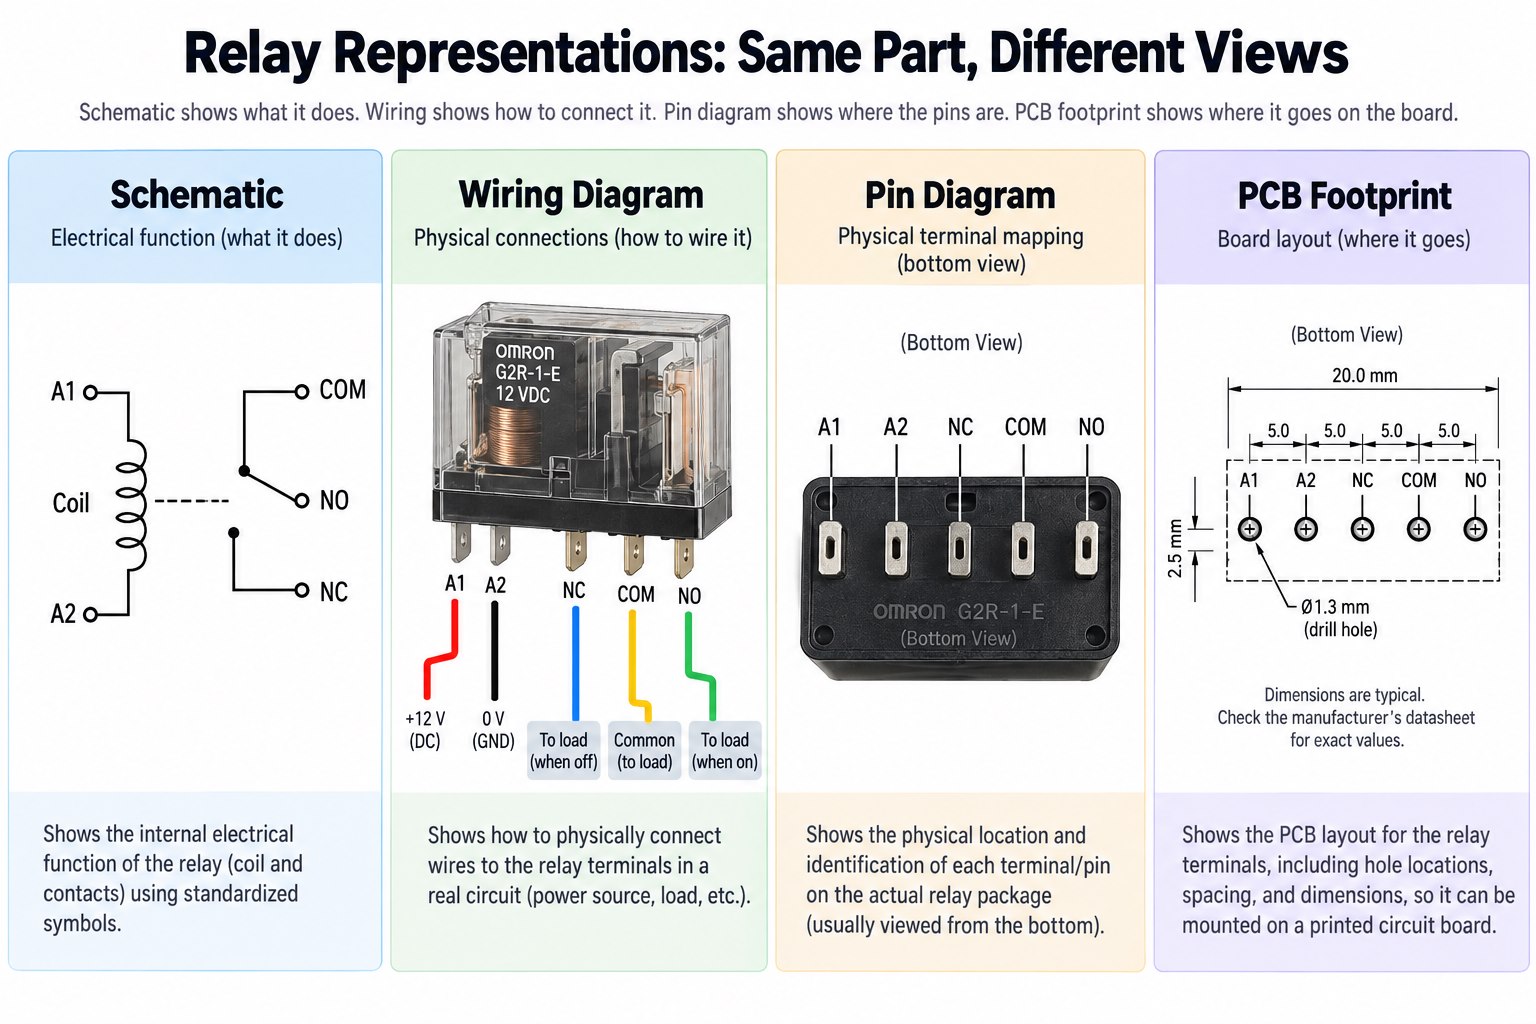
Relay Diagram vs Wiring Diagram vs Pin Diagram: What Is the Difference?

A relay schematic, wiring diagram, pin diagram, and PCB footprint answer different engineering questions.

Diagram Type Main Question It Answers
Relay schematic What does the relay do electrically?
Wiring diagram Where should each wire connect?
Pin diagram Which physical terminal performs each function?
Internal diagram How are the coil and contacts arranged?
PCB footprint Where are the actual pads or holes?

A schematic may show an SPDT relay as a coil plus COM, NO, and NC contacts. The wiring diagram then shows how those terminals connect to the power supply, switch, and load.

A relay pin diagram maps those functions to physical relay pins. Finally, the PCB footprint converts the mechanical package into copper pads or plated through holes.

Relay schematic wiring diagram pin diagram and PCB footprint comparison

What Should You Check Before Using a Relay Diagram for PCB Design?

Before placing a relay on a PCB, verify the physical pinout against the exact manufacturer datasheet rather than relying on a generic relay diagram.

Important checks include:

  • Datasheet drawing orientation
  • Top view versus bottom view
  • Coil pin locations
  • COM / NO / NC pin mapping
  • Coil voltage
  • Coil current
  • Internal suppression components
  • Contact current and voltage rating
  • Load type
  • Contact resistance
  • PCB hole size
  • Pad diameter
  • Relay body clearance

The coil also affects the surrounding circuit. A microcontroller normally cannot drive many relay coils directly, so the PCB may need a BJT or MOSFET driver, base or gate resistor, flyback diode, LED indicator, optocoupler, or separate relay supply rail.

For higher-voltage loads, creepage and clearance between the control side and switched contacts must also be reviewed. A correct schematic symbol can still produce a wrong PCB if the footprint is mirrored or the physical pinout is interpreted from the wrong viewing direction.

EBest Circuit can review relay footprints, driver circuits, through-hole assembly, isolation spacing, trace current capacity, and PCBA requirements during DFM before fabrication.

FAQ About Relay Diagrams

1. What does a relay diagram show?
A relay diagram shows the relationship between the coil and switching contacts, including functions such as COM, NO, and NC.

2. What do 85 and 86 mean on a relay?
They are commonly the coil terminals on standard automotive relays. The actual relay marking or datasheet should still be checked.

3. What is the difference between a 4-pin and 5-pin relay?
A common 4-pin automotive relay provides a normally-open switching path, while a common 5-pin changeover relay adds terminal 87a for the normally-closed path.

4. What is an 8-pin relay diagram?
An 8-pin relay is commonly a DPDT relay with two changeover contact sets and one coil. Physical pin numbering varies by model.

5. Does relay coil polarity matter?
Not always. Polarity becomes important when the relay contains an internal diode, LED, or another polarity-sensitive suppression circuit.

6. Can I use the same relay diagram for every relay with the same number of pins?
No. The same pin count can be used by relays with different contact forms, internal features, and physical pin assignments. Always verify the exact datasheet.

Designing a PCB Around a Relay?

A relay diagram explains the electrical switching function, but reliable PCB implementation also depends on the actual footprint, coil driver, suppression method, load current, isolation spacing, and assembly process.

EBest Circuit supports relay control PCB fabrication, through-hole and SMT assembly, DFM review, component sourcing, and functional testing. If you have a similar control-board project, send your Gerber files, BOM, schematic, and relay specifications to sales@bestpcbs.com for engineering review.

You may also like

PCB Test Coupons: Types, Testing & IPC Guide

September 17th, 2026

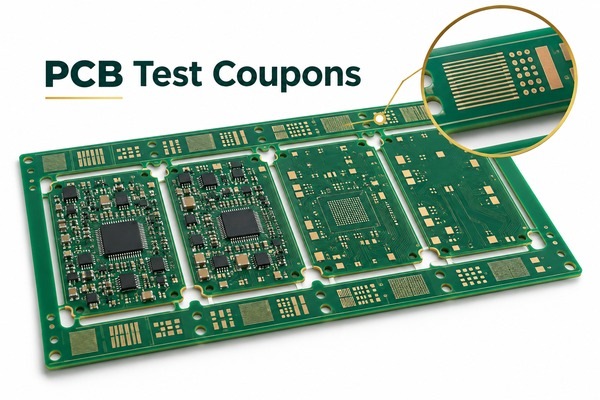
PCB test coupons are representative test structures placed on the same fabrication panel as the production boards. They are built with the same materials, copper plating, lamination, drilling, and other key processes so manufacturers can verify characteristics such as controlled impedance, plated-hole quality, via reliability, registration, and solderability without cutting into the finished PCB.

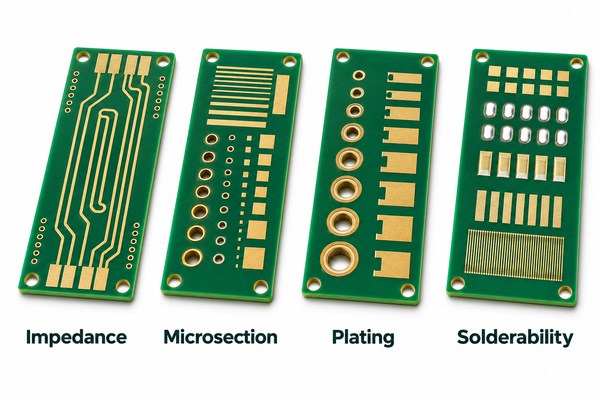
Different PCB test coupons serve different purposes. Impedance coupons are commonly checked with TDR, while structural coupons can be microsectioned to inspect plating and internal alignment. The coupon design should reflect the actual production stackup and fabrication process.

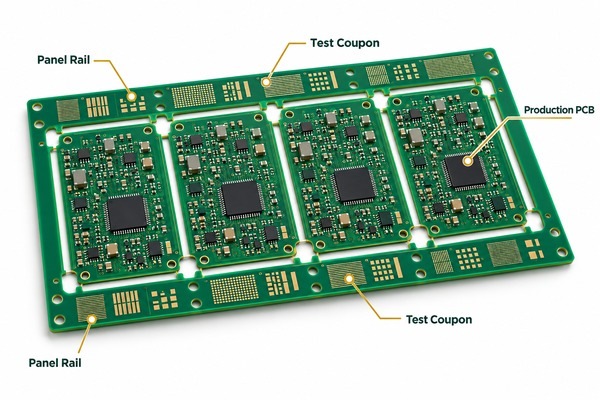
PCB test coupons integrated into the panel rail of a production PCB panel

What Is a PCB Test Coupon?

A PCB test coupon is a dedicated test structure manufactured on the same panel as the production PCB to represent selected features of the finished board.

Unlike the functional PCB, the coupon is created specifically for inspection or measurement. Depending on the requirement, it may reproduce:

  • Controlled-impedance traces
  • Plated through holes
  • Microvias or blind vias
  • Internal layer registration features
  • Copper plating structures
  • Solderability features

The key point is representation. A useful coupon should experience the same relevant fabrication processes as the board it is intended to represent.

PCB test coupons are commonly placed in the panel rail or other non-product area, so testing does not consume a usable PCB.

At EBest Circuit, coupon requirements can be reviewed together with the production stackup during DFM. For controlled-impedance, HDI, RF, or high-reliability boards, this helps keep the test structure aligned with the actual PCB manufacturing conditions.

Why Are Test Coupons Used Instead of Testing the Production PCB?

PCB test coupons allow measurements and destructive inspections to be performed without damaging the production board.

Some verification methods cannot be carried out conveniently on a finished PCB. Microsection analysis, for example, requires the sample to be cut, mounted, polished, and inspected under magnification.

Coupons also provide a more consistent structure for tests such as TDR because production routing may contain:

  • Vias
  • Pads
  • Connectors
  • BGA breakouts
  • Plane changes
  • Short trace segments

These features can make measurement results harder to interpret.

A dedicated coupon can reproduce the required stackup and trace geometry while providing enough length and accessible test points for repeatable measurement.

The coupon therefore does not replace electrical or functional testing of the PCB. It provides process evidence for specific fabrication characteristics.

What Types of PCB Test Coupons Are Commonly Used?

PCB test coupon types are usually selected according to what needs to be verified rather than by using one universal coupon design.

Coupon / Test Structure What It Checks Typical Test Method
Impedance coupon Single-ended or differential impedance TDR
PTH structural coupon Hole wall plating and registration Microsection
Via reliability coupon Via or interconnect integrity Thermal stress / resistance monitoring
Microvia coupon HDI microvia quality and stacking Microsection / reliability test
Solderability coupon Solder wetting performance Solderability test
Peel-strength coupon Copper adhesion Peel test
SIR coupon Surface insulation resistance Electrical resistance testing

Some IPC qualification and conformance structures use letter-based coupon designations. However, for most PCB buyers and engineers, the more useful question is not the letter itself but what manufacturing characteristic the coupon is intended to verify.

Common PCB test coupon types including impedance plated through-hole microvia via reliability solderability and SIR coupons

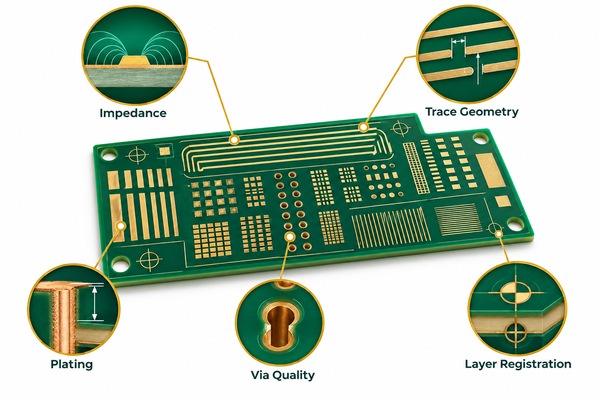
What Can PCB Test Coupons Verify?

PCB test coupons can verify several manufacturing characteristics that are difficult to confirm from visual inspection alone.

Common checks include:

  • Controlled impedance
  • Copper plating thickness
  • Plated through-hole integrity
  • Microvia quality
  • Annular ring condition
  • Internal layer registration
  • Solderability
  • Copper adhesion
  • Interconnect reliability

For example, an impedance coupon can confirm whether a nominal 50 Ω or 100 Ω structure is within tolerance after lamination, plating, and etching.

A microsection coupon serves a different purpose. It allows the manufacturer to inspect the actual cross-section of a plated hole or via and evaluate conditions such as copper distribution, registration, and interface quality.

PCB test coupon illustrating impedance trace geometry plating via quality and layer registration verification

Where Are Test Coupons Located on a PCB Panel?

PCB test coupons are usually placed in the panel rail or another non-functional area of the production panel.

This position allows the coupon to travel through the same major fabrication processes as the PCBs while remaining separate from the customer’s usable board outline.

A useful coupon should be positioned so that it represents the production process as closely as practical, especially for:

  • Lamination
  • Drilling
  • Copper plating
  • Etching
  • Surface treatment

Coupon placement also needs to leave enough room for test access, sectioning, or removal from the panel.

For controlled-impedance production, the coupon is typically designed around the same layer pair, dielectric thickness, copper condition, and trace geometry used by the actual impedance-controlled routing.

PCB panel showing test coupons located in the top and bottom panel rails

How Are Impedance Test Coupons Tested with TDR?

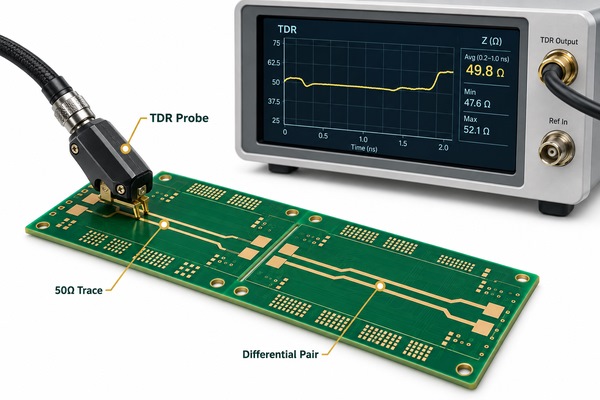
An impedance test coupon reproduces the controlled-impedance structure of the production PCB so its characteristic impedance can be measured with time-domain reflectometry, or TDR.

The coupon normally represents the same:

  • Signal layer
  • Reference plane
  • Dielectric thickness
  • Copper thickness
  • Trace width
  • Differential spacing, where applicable
  • Material system

During TDR testing, a fast electrical edge is launched into the coupon. The instrument measures reflections along the transmission line and converts them into an impedance profile.

The result is then compared with the specified target, such as:

  • 50 Ω single-ended
  • 90 Ω differential
  • 100 Ω differential

A typical tolerance may be ±10%, although tighter limits can be specified.

The coupon should be based on the final production stackup rather than only the original CAD trace width. Plating, etching, dielectric thickness, and manufacturing compensation can all change the finished impedance.

PCB impedance test coupon connected to TDR equipment for controlled impedance verification

How Are Test Coupons Used for Microsection and Via Inspection?

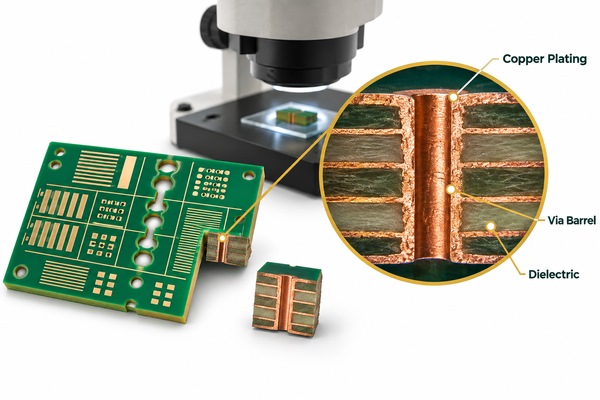
Microsection coupons are cut and polished so the internal PCB structure can be inspected directly under magnification.

This method is commonly used to evaluate plated through holes, blind vias, microvias, and multilayer registration.

A typical microsection can reveal:

  • Hole-wall copper thickness
  • Copper distribution
  • Annular ring condition
  • Layer-to-hole registration
  • Resin condition
  • Via interfaces
  • Microvia geometry
  • Lamination quality

Because the coupon is intentionally sacrificed, the production PCB remains intact.

For HDI boards, microsection inspection is especially useful because microvias, stacked structures, and thin dielectric layers can create manufacturing risks that are not visible from the board surface.

Microsection results should be interpreted against the relevant drawing, customer specification, and applicable IPC acceptance requirements rather than treated as a generic pass/fail image.

PCB microsection showing plated through hole microvia copper layers annular ring and resin

Who Should Design PCB Test Coupons—the Designer or the Fabricator?

PCB test coupon design is typically a shared responsibility: the PCB designer defines the electrical and reliability requirements, while the fabricator finalizes the coupon structure for the actual production process.

The customer should provide requirements such as:

  • Target impedance
  • Impedance tolerance
  • Stackup constraints
  • Material requirement
  • Via structure
  • Reliability requirement
  • Required reports or inspection records

The fabricator then knows the actual production details, including dielectric availability, drill size, finished copper thickness, plating allowance, and etching compensation.

For that reason, it is often better for the PCB manufacturer to create or adjust the coupon after the production stackup is confirmed.

If a customer-supplied coupon is included in the fabrication data, it should still be reviewed during DFM to make sure it matches the manufacturing stackup and test method.

Engineer reviewing PCB stackup impedance and test coupon requirements during DFM

What Test Coupon Requirements Should You Include in Your PCB RFQ?

A PCB RFQ should clearly state what needs to be verified rather than simply asking for “test coupons.”

For controlled-impedance or high-reliability projects, provide:

  • Gerber or ODB++ files
  • PCB stackup or stackup constraints
  • Material grade
  • Finished board thickness
  • Copper weight
  • Target impedance
  • Single-ended or differential requirement
  • Impedance tolerance
  • Critical routing layers
  • Via or microvia structure
  • Required test reports
  • Whether physical coupons should be returned

For example, “50 Ω controlled impedance required” is less useful than specifying the routing layer, reference plane, stackup requirement, and tolerance.

FAQ About PCB Test Coupons

1. Is a PCB test coupon part of the finished PCB? No. It is normally placed in the panel rail or another non-product area and removed from the production panel.

2. Do I need to include a test coupon in my Gerber files? Not always. In many projects, the customer provides the test requirement and the PCB manufacturer creates the coupon based on the final production stackup.

3. What is an impedance test coupon? It is a representative transmission-line structure used to measure the finished PCB impedance, commonly with TDR.

4. Can a test coupon prove that every PCB on the panel is good? No. A coupon provides representative process evidence for specific characteristics. It does not replace board-level inspection or electrical testing.

5. Are PCB test coupons normally sent to the customer? They can be. Whether physical coupons, TDR reports, microsection images, or other records are supplied should be defined in the order or quality requirement.

6. What information should I provide for controlled-impedance coupon testing? Provide the target impedance, tolerance, routing layer, reference plane, stackup, material, copper weight, and any special coupon or reporting requirements.

Ready to Review Your PCB Test Coupon Requirements?

PCB test coupons are most useful when they are tied to a specific manufacturing risk, whether that is impedance, plating, microvia quality, registration, or another measurable characteristic. Defining the test requirement before production makes the coupon more representative and the resulting data more useful.

EBest Circuit supports controlled-impedance, HDI, RF, multilayer PCB manufacturing, PCBA, DFM review, TDR testing, and microsection inspection. For projects that require coupon-based verification, send your Gerber files and PCB specifications to sales@bestpcbs.com. Our engineering team can review the stackup, test requirements, and coupon approach before fabrication.

After coupon results are approved, our SMT assembly workflow can also coordinate circuit board stencil requirements with the released fabrication data.

You may also like

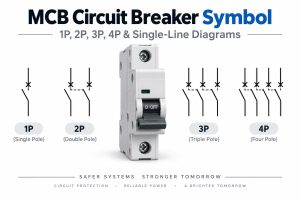
MCB Circuit Breaker Symbol: 1P, 2P, 3P, 4P & Single-Line Diagrams

September 17th, 2026

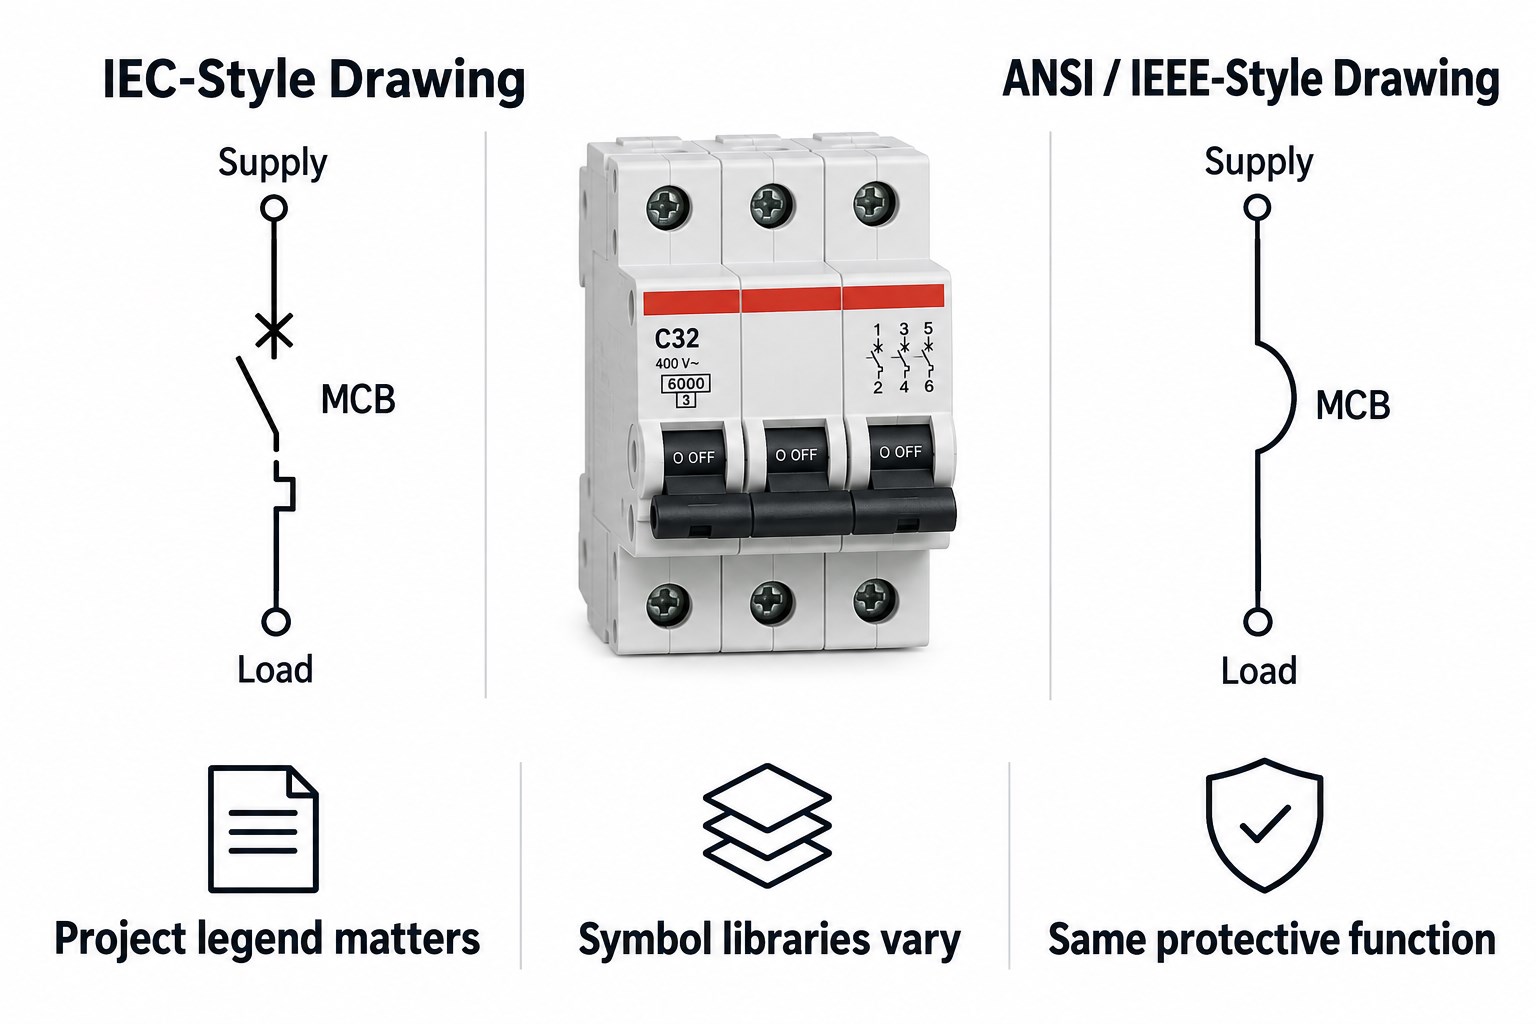
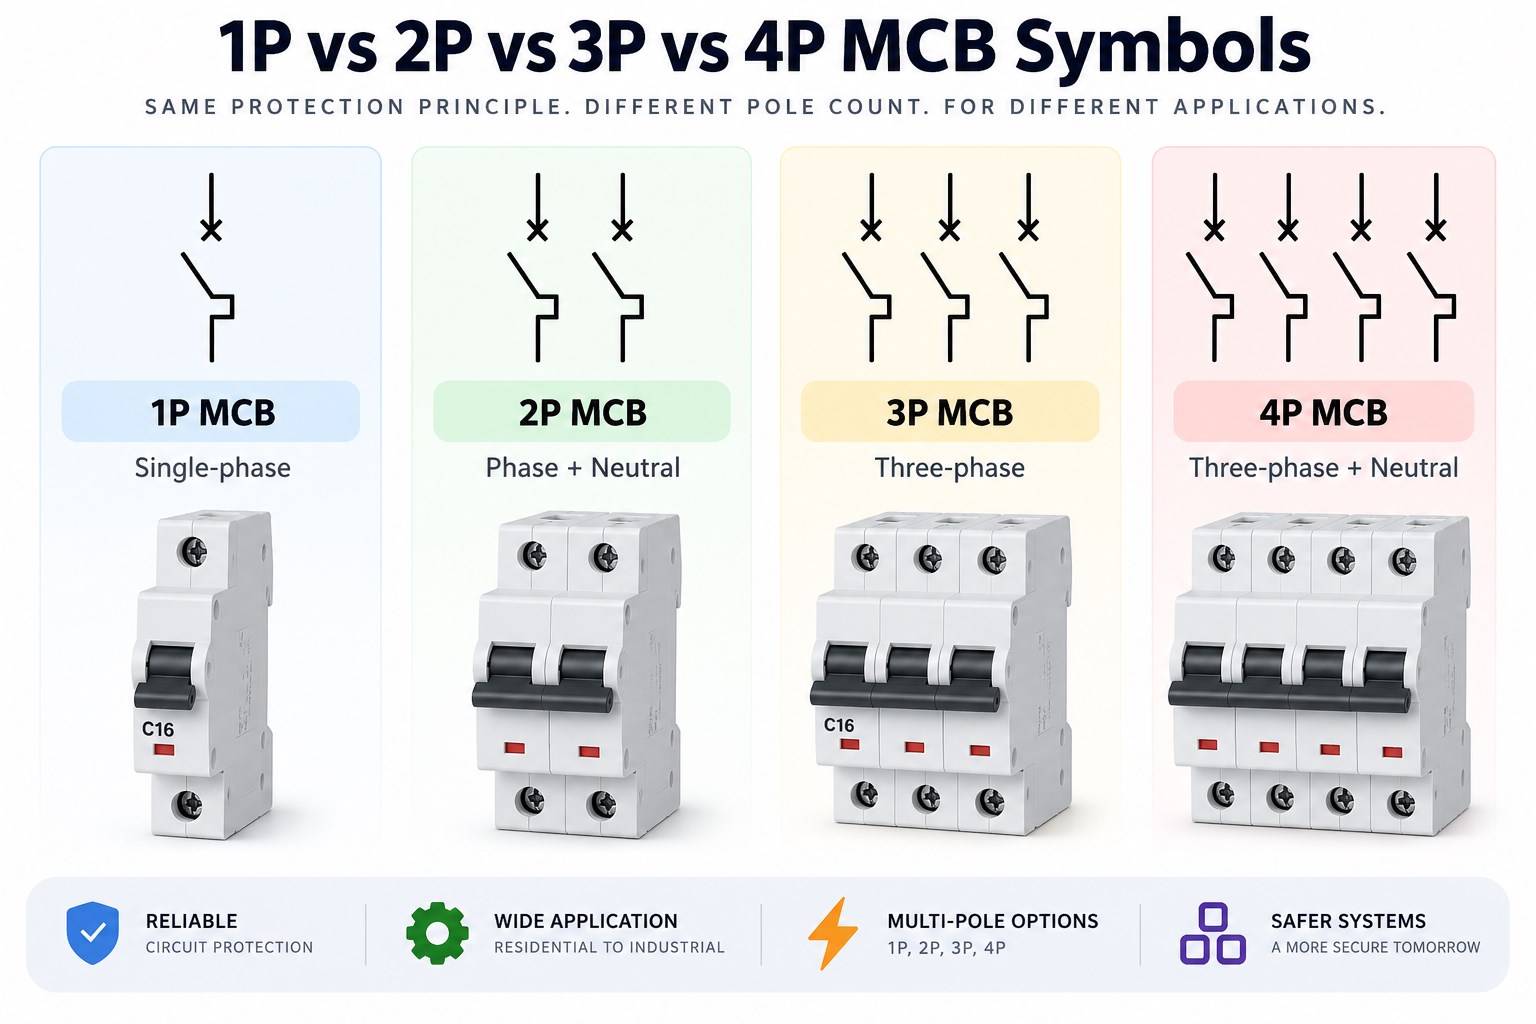
An MCB symbol looks simple, but reading it correctly requires more than recognizing a breaker-shaped graphic. A drawing may use IEC conventions, ANSI/IEEE-style symbols, manufacturer-specific CAD libraries, or a simplified symbol created for a single-line diagram. The same protective function can therefore appear differently from one project to another.

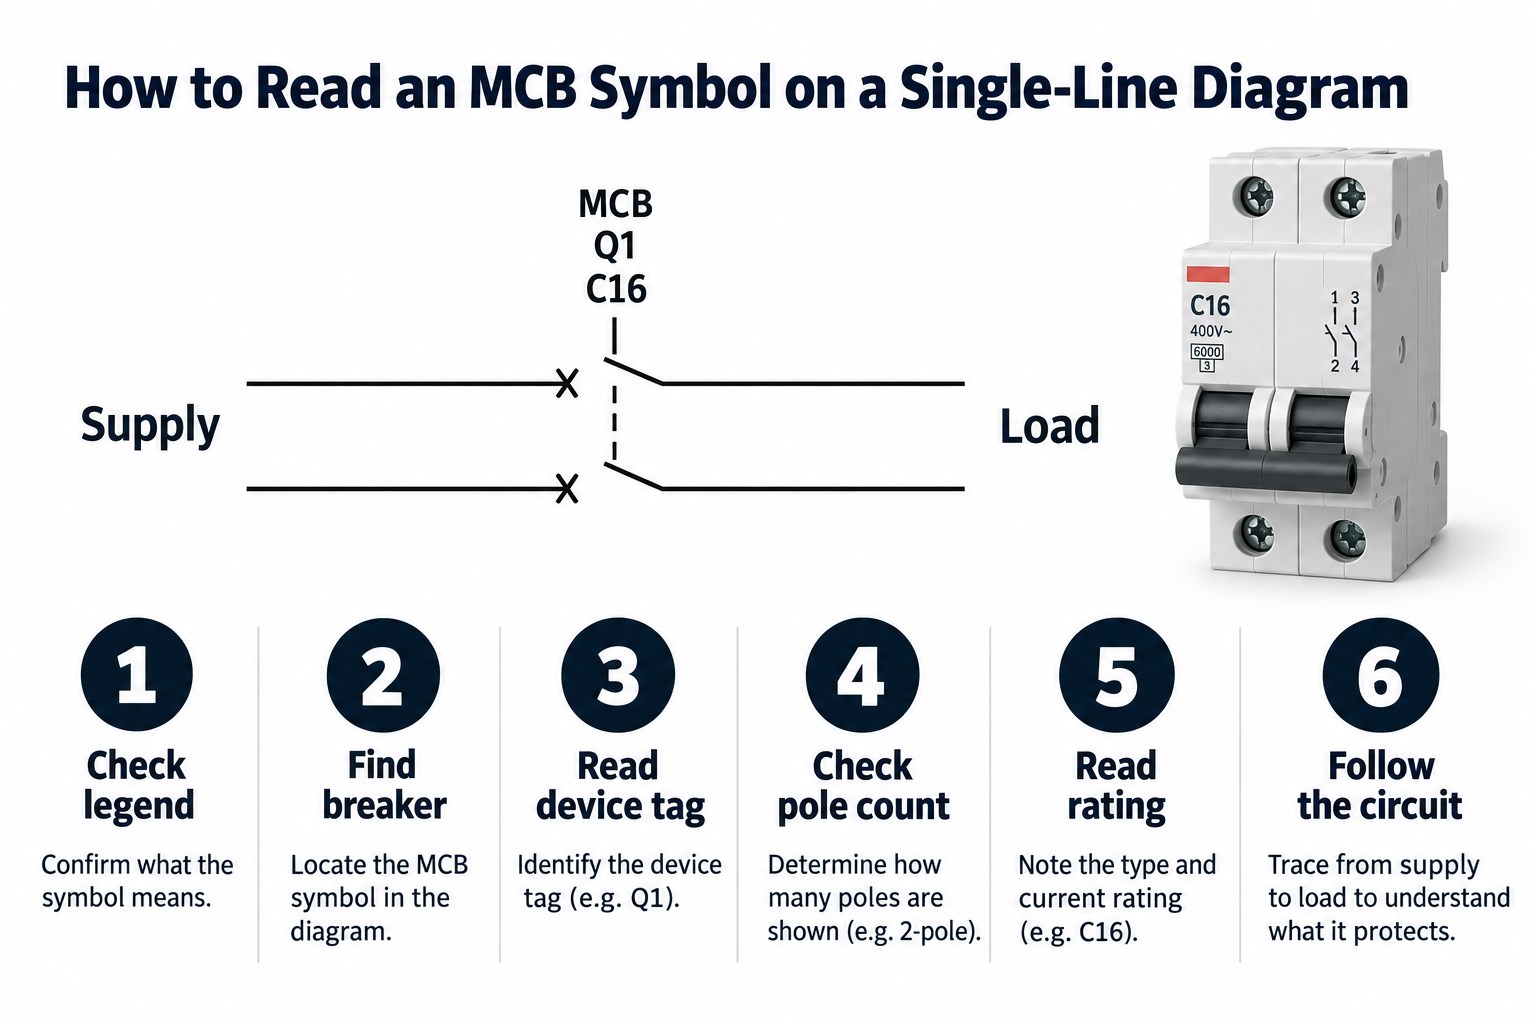
The practical approach is to treat the symbol as one piece of information. Pole count, device tag, current rating, trip characteristic, breaking capacity, and the project legend complete the picture. This becomes especially important when distinguishing 1P, 2P, 3P, 4P, MCB, MCCB, and other protective devices.

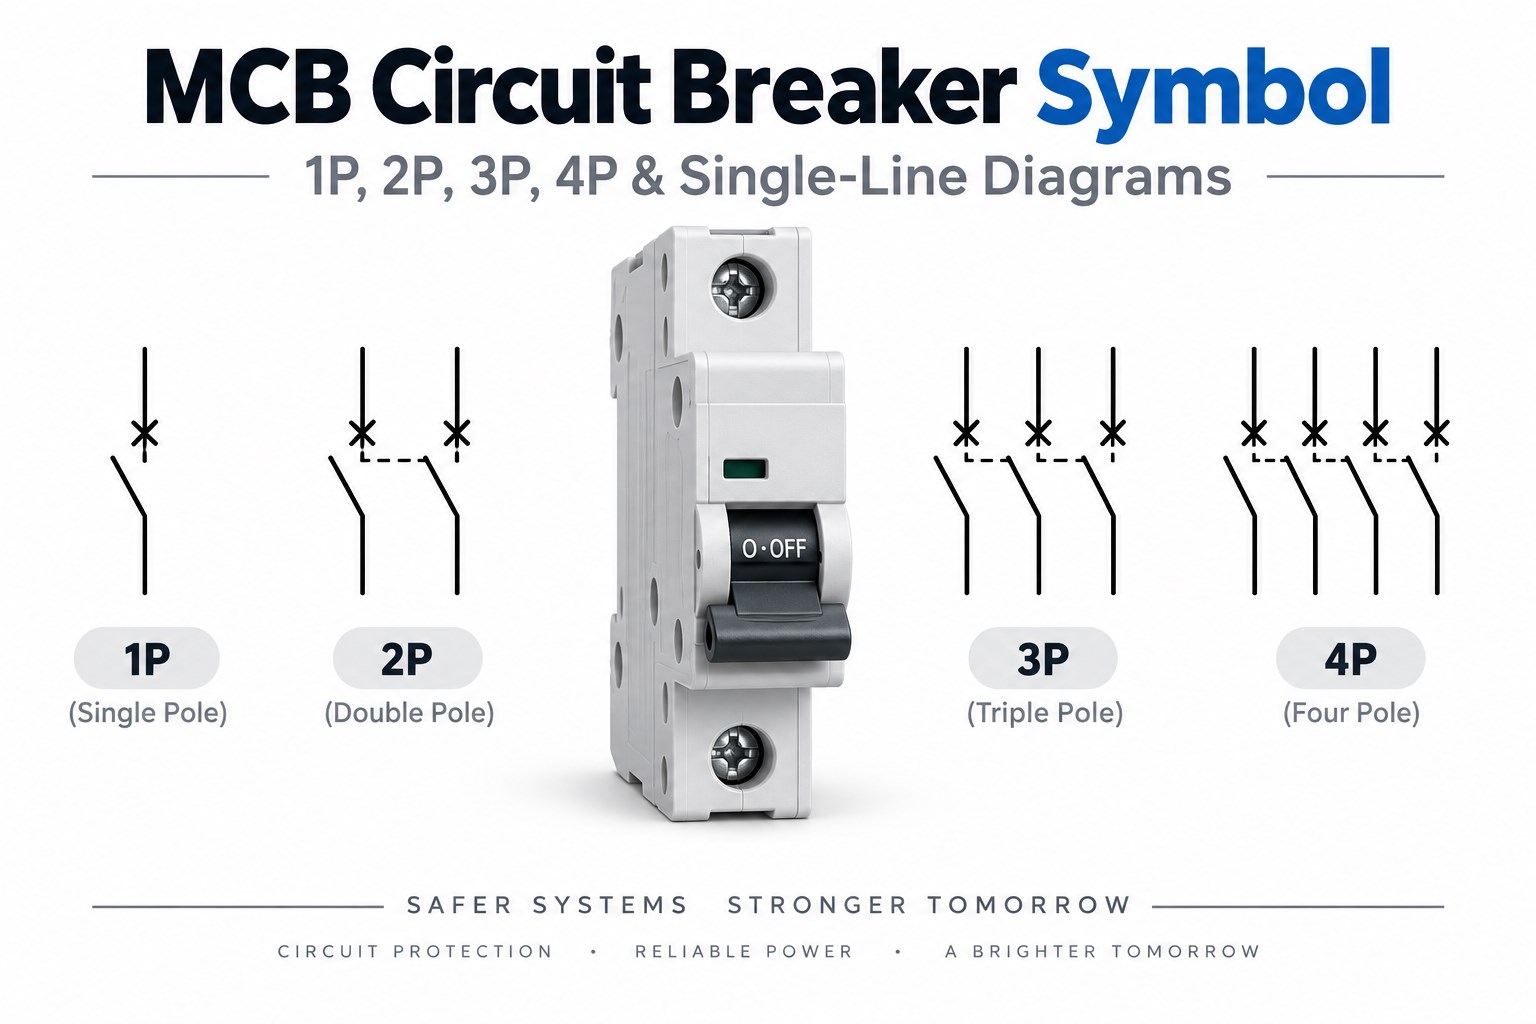
MCB circuit breaker symbol guide showing 1P 2P 3P 4P and single-line diagram

Key Takeaways

  • An MCB circuit breaker symbol represents a miniature circuit breaker used mainly for overload and short-circuit protection, but the exact graphic can vary by drawing standard and diagram type.
  • There is no single MCB symbol that appears identically on every schematic. IEC, ANSI/IEEE-style drawings, CAD libraries, and project legends may use different representations.
  • 1P, 2P, 3P, and 4P MCB symbols mainly indicate how many conductors are switched together. 1P+N and 3P+N configurations need additional attention because the neutral pole may be switched without having the same protective function as the phase poles.
  • A three-phase MCB may appear as three mechanically linked contacts on a detailed schematic, but a single-line diagram can represent the same three-pole breaker with one compact symbol.
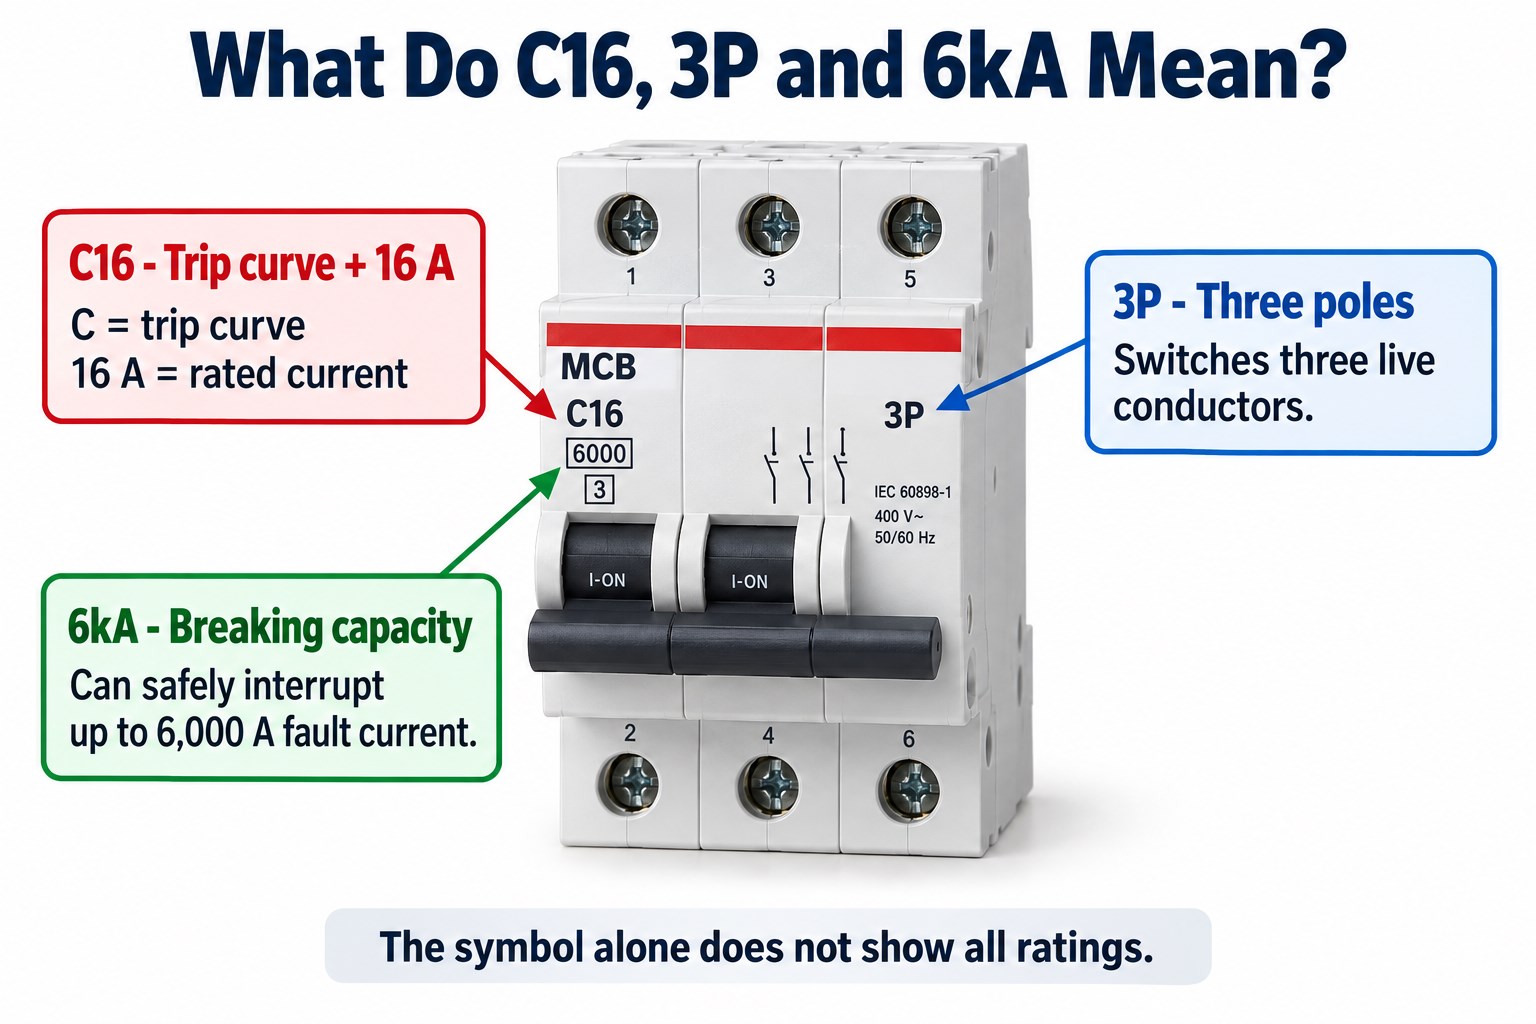
  • The symbol alone usually does not tell you the current rating, trip curve, breaking capacity, AC/DC suitability, or exact product type.
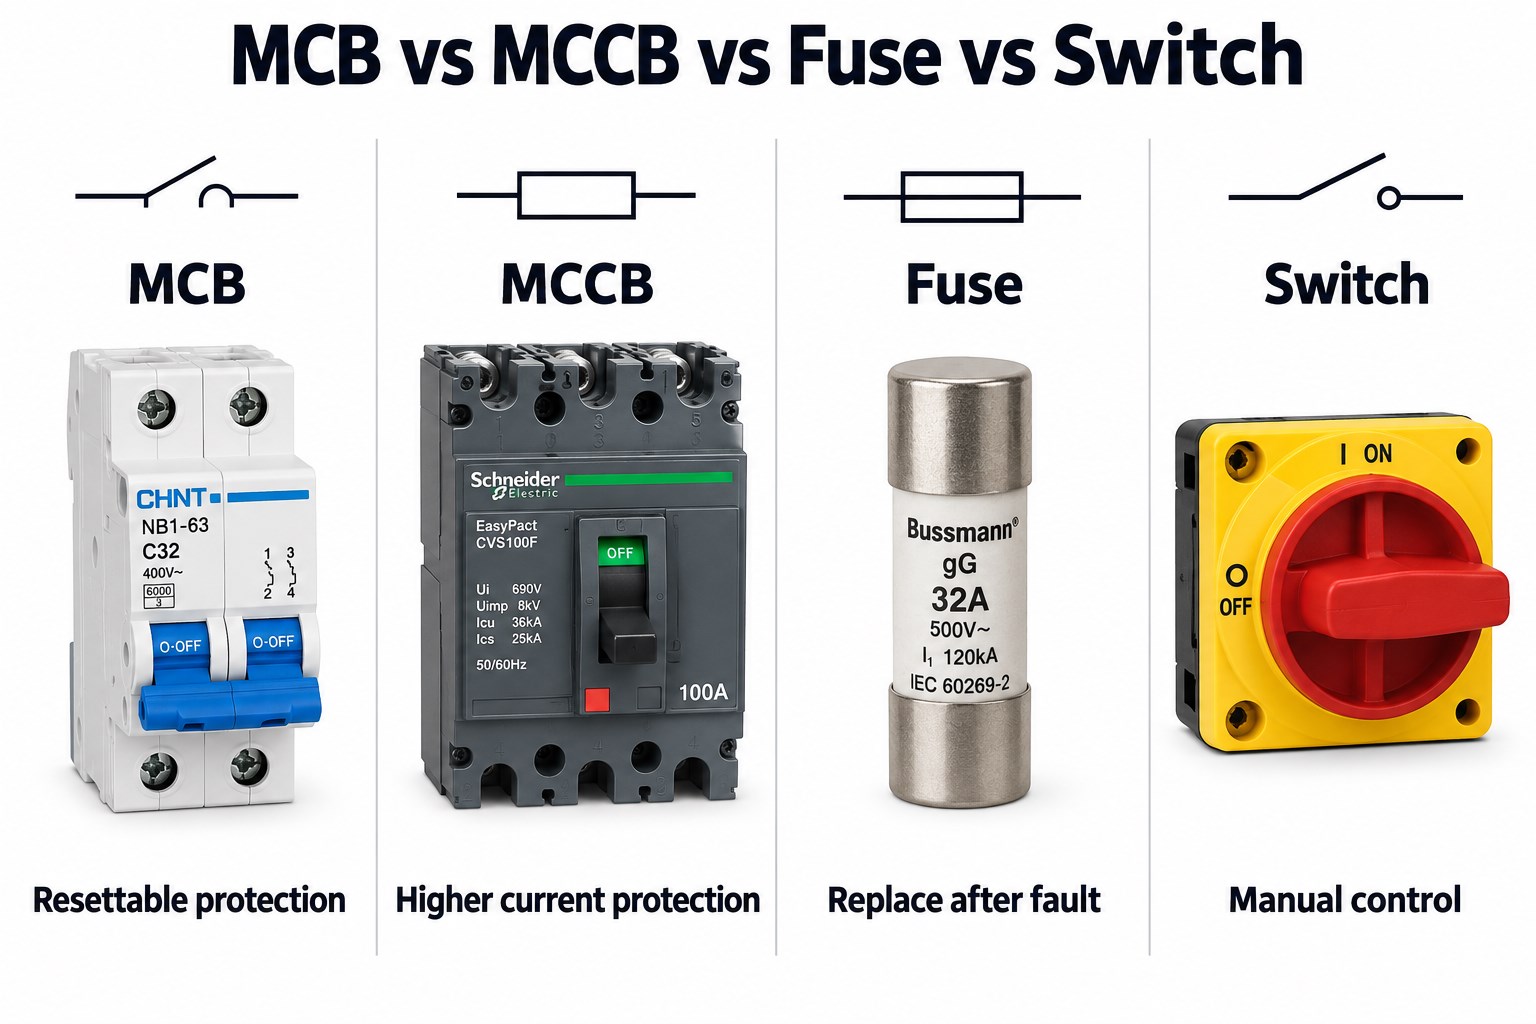
  • MCB and MCCB symbols can look similar on simplified diagrams. Device tags, ratings, schedules, and specifications are often needed to tell them apart.
  • When reading an electrical drawing, always use the project legend, pole annotation, breaker tag, and ratings together rather than identifying the device from shape alone.

What Does MCB Mean and What Does an MCB Do?

MCB stands for Miniature Circuit Breaker. It is an automatically operated protective switching device commonly used to interrupt a circuit when an overload or short circuit exceeds the breaker’s operating limits.

Unlike a fuse, an MCB can normally be reset after the fault has been cleared. It also provides manual switching, although its primary role in the circuit is protection rather than routine control.

Typical MCB applications include:

  • Residential distribution boards
  • Commercial branch circuits
  • Lighting circuits
  • Small motors
  • Control panels
  • Industrial auxiliary circuits
  • Equipment power distribution

The exact protection characteristics depend on the device. Rated current, trip curve, breaking capacity, voltage rating, and pole configuration must therefore be checked separately from the schematic symbol.

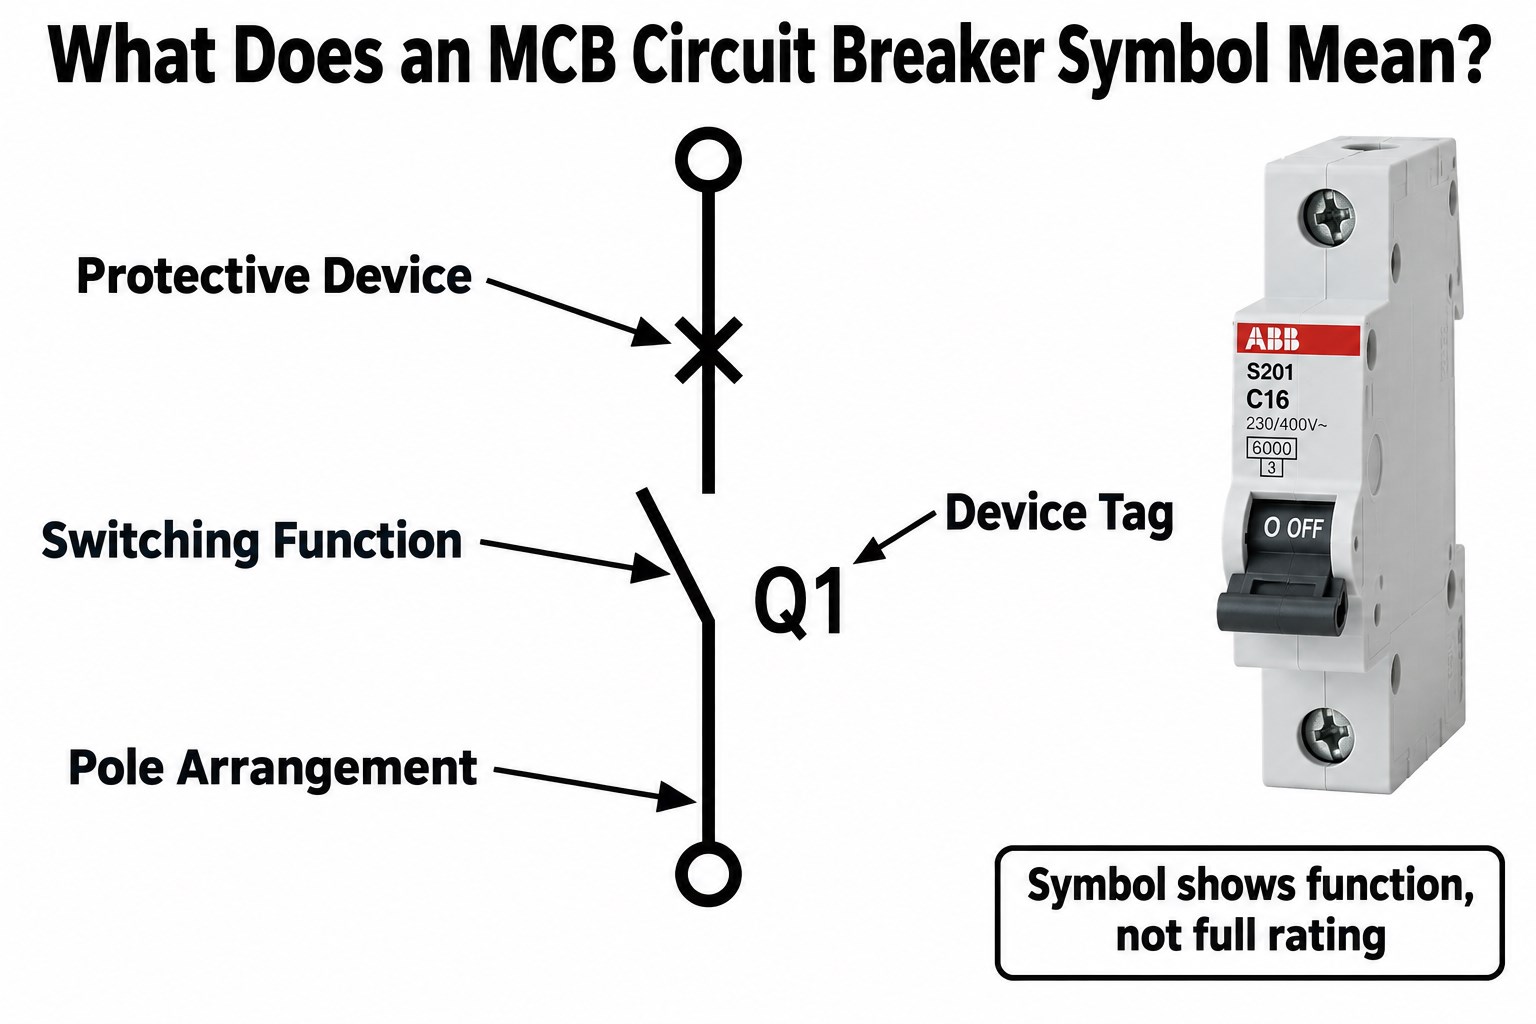
What Does an MCB Circuit Breaker Symbol Mean?

The MCB symbol meaning is that the circuit contains a protective switching device capable of automatically interrupting fault current.

Depending on the drawing style, the symbol may show a switching contact, a break in the conductor path, a protective-device qualifier, multiple mechanically linked poles, or a device tag such as CB1, QF1, or MCB1.

The graphic can help identify the function and sometimes the pole arrangement, but it usually does not provide the complete device specification. Rated current, trip curve, breaking capacity, voltage, AC/DC suitability, manufacturer, product series, and terminal arrangement normally come from annotations, schedules, or the component specification.

MCB symbol meaning showing protective device switching function pole arrangement and device tag

Is There One Standard MCB Symbol?

No. There is no single MCB graphic that appears identically in every electrical schematic, single-line diagram, and CAD library.

IEC 60617 provides standardized graphical symbols for electrical diagrams, including switching and protective functions. However, the symbol actually shown in a project can vary depending on how the standard is applied and how much detail the drawing needs.

Variation can come from IEC-based symbol libraries, ANSI/IEEE-style drawings, single-line diagrams, detailed control schematics, CAD software libraries, company drafting standards, and manufacturer documentation.

The correct method is therefore to check the drawing legend and project drafting standard first. A symbol should be interpreted in the context of the drawing in which it appears.

IEC vs ANSI/IEEE MCB Symbols: What Is the Difference?

IEC and ANSI/IEEE-style drawings can represent circuit-breaker functions differently, although both communicate the same basic idea: a protective device that can open the electrical path.

Drawing Convention Typical Characteristics
IEC IEC 60617 graphical conventions, IEC-style device designations
ANSI/IEEE North American symbol conventions and device numbering
Single-line diagram Simplified representation of multiphase circuits
Detailed schematic Individual contacts, coils, mechanical links, and terminals may be shown

Neither system changes what the MCB physically does. The main risk is assuming a symbol copied from one standard must look exactly the same in another drawing. In real engineering documentation, the project legend remains the safest reference.

IEC versus ANSI IEEE style MCB circuit breaker symbol comparison

1P vs 2P vs 3P vs 4P MCB Symbols: What Changes?

The main difference between 1P, 2P, 3P, and 4P MCB symbols is the number of conductors operated together by the breaker.

MCB Configuration Conductors Switched Typical Application
1P 1 Single-phase branch circuit
2P 2 Phase + neutral or two-line circuit
3P 3 Three-phase circuit
4P 4 Three-phase + neutral
1P+N 2 Single-phase with switched neutral
3P+N 4 Three-phase with switched neutral

A 1P MCB normally interrupts one live conductor. A 2 pole MCB symbol represents two mechanically linked poles operating together, while a 3P MCB mechanically links three poles for a three-phase system. A 4 pole MCB symbol adds a fourth switched path, commonly used when the neutral must also be disconnected.

However, 1P+N and 3P+N should not automatically be treated as identical to 2P and 4P protective devices. In some constructions, the neutral pole is switched but does not provide the same overcurrent protection as the phase pole.

1P 2P 3P and 4P MCB symbols with corresponding breaker configurations

What Does a 3-Phase Circuit Breaker Symbol Show?

A 3 phase circuit breaker symbol represents one breaker operating across all three phase conductors together.

In a detailed schematic, the drawing may show three separate contacts with a mechanical linkage between them. That linkage indicates that the poles operate together as one device.

In a single-line diagram, however, the entire three-phase circuit is represented by one line. The breaker may therefore appear as one compact symbol with annotations such as 3P, 3Ø, CB1, QF1, C32, or 10 kA.

A single line in an SLD does not mean the breaker has only one pole. Mechanical linkage shows simultaneous operation; it is not another current-carrying wire.

How Do You Read an MCB Symbol on a Single-Line Diagram?

Reading an MCB on a single-line diagram is easier when you follow the information in a fixed order instead of relying on the symbol shape alone.

  1. Check the drawing legend. Confirm what the project uses for MCBs, MCCBs, isolators, fuses, and switches.
  2. Locate the breaker symbol. Follow the incoming supply or feeder until you reach the protective switching device.
  3. Read the device tag. Common tags include MCB1, CB1, QF1, or Q1.
  4. Check the pole configuration. Look for 1P, 2P, 3P, 4P, 1P+N, or 3P+N.
  5. Read the current and trip information. A label such as C16 commonly indicates a C-characteristic 16 A MCB.
  6. Check breaking capacity and voltage. Values such as 6 kA or 10 kA describe short-circuit interruption capability under the applicable rating conditions.
  7. Follow the circuit upstream and downstream. Confirm where the breaker receives power and which load, bus, or subcircuit it protects.
How to read an MCB symbol on a single-line diagram step by step

What Do MCB Labels Such as C16, 3P and 6kA Mean?

MCB labels provide electrical information that the schematic symbol itself usually cannot communicate.

Marking Typical Meaning
C C-type tripping characteristic
16 16 A rated current
3P Three-pole device
6 kA Rated short-circuit breaking capacity under the applicable rating standard

A B, C, or D designation normally relates to the magnetic trip characteristic rather than the number of poles. Similarly, 6 kA does not mean the breaker is intended to carry 6,000 A continuously. It describes the short-circuit current the device is rated to interrupt under specified test conditions.

MCB marking explanation for C16 3P and 6kA

MCB vs MCCB Symbols: Can You Tell Them Apart by Shape?

Not always. An MCB and an MCCB can share a generic circuit-breaker symbol in simplified drawings because both perform the same basic protective switching function.

The difference may only become clear from surrounding information. Check the device tag, MCB/MCCB annotation, rated current, frame size, breaking capacity, adjustable trip settings, electronic or thermal-magnetic trip unit, equipment schedule, and manufacturer part number.

An MCCB is generally used for higher current levels and more demanding distribution applications, while an MCB is typically used for lower-current final or branch circuits. However, symbol shape alone should not be used to determine the product category.

MCB vs Fuse vs Switch Symbol: How Do You Avoid Misreading Them?

MCBs, fuses, and switches can all interrupt a circuit, but their functions are different.

Device Automatic Fault Protection Resettable Main Purpose
MCB Yes Yes Overload / short-circuit protection
MCCB Yes Yes Higher-current protective switching
Fuse Yes No Overcurrent protection
Switch Not necessarily Yes Manual switching

An MCB combines switching with automatic overcurrent protection. A fuse also provides automatic protection, but once its element melts, the fuse must be replaced. A normal switch can open the circuit manually but should not be assumed to provide overload or short-circuit protection unless it is part of a protective device.

MCB MCCB fuse and switch symbol and device comparison

What Information Should Be Checked Beyond the MCB Symbol?

The MCB symbol identifies the device function, but selecting or verifying the physical breaker requires more information.

Engineers should check:

  • Rated current
  • Pole count
  • Rated voltage
  • AC or DC operation
  • Trip characteristic
  • Breaking capacity
  • Frequency
  • Installation category
  • Terminal arrangement
  • Applicable standard
  • Manufacturer and part number

The same distinction matters when an MCB connects to a PCB-based control system. The schematic symbol is not the physical footprint.

A control PCB may interface with auxiliary contacts, shunt-trip coils, undervoltage release, remote actuators, current sensors, status inputs, or DIN-rail terminal blocks. Connector pitch, terminal current, creepage, clearance, relay ratings, and isolation barriers must therefore be designed from the actual hardware specification rather than from the MCB symbol shown in the system schematic.

FAQ About MCB Circuit Breaker Symbols

1. What is the full form of MCB?
MCB stands for Miniature Circuit Breaker. It is mainly used for automatic overload and short-circuit protection in lower-current electrical circuits.

2. What is the symbol of an MCB?
The exact symbol depends on the drawing standard and diagram type. IEC-based schematics, ANSI/IEEE-style drawings, and single-line diagrams may represent the breaker differently, so the project legend should be checked.

3. What is the difference between a 1P and 2P MCB symbol?
A 1P MCB operates one conductor, while a 2P MCB operates two mechanically linked conductors together.

4. What is the symbol for a 3-phase MCB?
A detailed schematic may show three mechanically linked breaker contacts. In a single-line diagram, one breaker symbol marked 3P may represent the complete three-phase device.

5. Is the MCB symbol different from the MCCB symbol?
Not necessarily. Simplified electrical drawings can use the same basic circuit-breaker symbol for both, with annotations or schedules identifying whether the device is an MCB or MCCB.

6. Can an MCB symbol tell me whether the breaker is AC or DC?
Usually not. AC/DC suitability should be confirmed from the rating annotation, project specification, and manufacturer datasheet rather than inferred from the symbol shape.

Reading an MCB Symbol on a PCB-Based Control System?

An MCB symbol can identify the protective device on the electrical schematic, but PCB design requires the actual breaker interface to be reviewed separately. Auxiliary contacts, control voltages, terminal spacing, isolation, relay outputs, and sensing circuits all affect the final board.

EBest Circuit supports industrial control PCB fabrication, DFM review, component sourcing, PCBA, and functional testing. If your control-board project interfaces with breakers, relays, contactors, or other power devices, send your Gerber files, BOM, schematic, and electrical requirements to sales@bestpcbs.com for engineering review.

You may also like

STM32 vs ESP32: Performance, Power, Price & Which to Choose

September 17th, 2026

STM32 vs ESP32 is not a comparison between two individual chips. STM32 is a large Arm Cortex-M microcontroller family covering entry-level control through high-performance embedded processing, while ESP32 is a family of connected MCUs and SoCs designed around integrated wireless capability, general-purpose processing, and rapid IoT development.

This STM32 vs ESP32 microcontroller comparison focuses on production decisions rather than development-board popularity.

The better choice depends on the actual workload. CPU performance, peripherals, wireless requirements, power budget, unit cost, software ecosystem, PCB design, and production volume can all change the decision. Comparing representative devices such as STM32F103, STM32F4, STM32H7, classic ESP32, and ESP32-S3 gives a more useful picture than comparing the two brand families as if each contained only one MCU.

STM32 vs ESP32 comparison showing development boards and embedded applications

Key Takeaways

  • STM32 is usually a stronger starting point for deterministic control, motor control, industrial interfaces, and applications that need a wide MCU selection.
  • ESP32 is attractive for Wi-Fi, Bluetooth, IoT, and connected products because wireless connectivity is integrated into many ESP32 variants.
  • Performance depends on the exact devices being compared. STM32F103, STM32F4, STM32H7, classic ESP32, and ESP32-S3 belong to very different performance levels.
  • STM32 often fits low-power control applications well, while ESP32 power consumption depends heavily on radio activity, sleep strategy, and communication duty cycle.
  • ESP32 can reduce total BOM cost in wireless products by eliminating a separate Wi-Fi or Bluetooth module.
  • Robotics and drones do not have one universal winner. Real-time control and wireless communication place different demands on the MCU.
  • STM32 and ESP32 can also work together, with one handling deterministic control and the other handling wireless connectivity.

STM32 vs ESP32: What Is the Main Difference?

The main difference is positioning: STM32 is primarily a broad embedded-control MCU family, while ESP32 is strongly oriented toward connected embedded systems with integrated Wi-Fi and Bluetooth on many variants.

STM32 devices span many performance and application classes. Depending on the series, designers can choose different CPU cores, clock speeds, memory sizes, timers, ADCs, communication peripherals, security features, and low-power modes.

ESP32 devices combine MCU processing with wireless functionality in a compact platform. Typical strengths include:

  • Wi-Fi and Bluetooth integration
  • Large developer ecosystem
  • FreeRTOS support
  • Flexible GPIO
  • SPI, UART, I²C, ADC, PWM, and other common interfaces
  • Module options with flash and antenna already integrated

For products centered on motor control, precise timing, industrial I/O, or tightly managed low-power operation, STM32 is often a natural starting point. For connected sensors, gateways, smart devices, and Wi-Fi/Bluetooth products, ESP32 can simplify the architecture.

STM32 control focused versus ESP32 connectivity focused comparison

Which STM32 and ESP32 Models Should You Actually Compare?

A useful STM32 vs ESP32 comparison needs representative devices from similar application levels. Comparing STM32H7 directly with an older ESP32 while ignoring the intended workload can create misleading conclusions.

STM32 Family ESP32 Family Useful Comparison
STM32F103 Classic ESP32 Entry-level and older mainstream embedded designs
STM32F4 ESP32 / ESP32-S3 General embedded processing
STM32H7 ESP32-S3 Higher-performance applications
STM32WB55 ESP32 family Wireless embedded designs

STM32F103 is widely associated with low-cost development boards such as the Blue Pill, while STM32F4 is a common step up for DSP, control, and higher-performance applications.

STM32H7 moves into a much higher performance class with faster Cortex-M7 devices and stronger memory and peripheral architectures. ESP32-S3, meanwhile, improves processing and AI-oriented instruction support while keeping Wi-Fi and Bluetooth integration.

The right comparison should therefore start from application requirements, not family names.

STM32F103 STM32F4 STM32H7 and STM32WB55 compared with ESP32 and ESP32-S3 development boards

STM32 vs ESP32 Performance: Which Is Faster?

Neither platform is always faster because CPU performance depends on the exact STM32 and ESP32 devices being compared.

For an STM32 vs ESP32 speed comparison, benchmark the exact parts under the real workload. An STM32 vs ESP32 clock speed figure alone does not predict interrupt latency, peripheral throughput, or control-loop behavior.

Important factors include:

  • CPU architecture
  • Clock frequency
  • Number of cores
  • FPU and DSP support
  • Cache architecture
  • Internal RAM
  • External-memory support
  • DMA capability
  • Hardware accelerators
  • Interrupt and real-time behavior

An STM32F103 and STM32H7 are both STM32 devices, yet their performance levels are far apart. The same issue appears within the ESP32 family, where classic ESP32, ESP32-S3, C-series, and other variants use different architectures and peripheral sets.

ESP32 can perform well when parallel tasks, networking, or connected applications are important. Higher-end STM32 devices can offer stronger deterministic processing for control loops, signal processing, and demanding embedded workloads.

Clock speed alone should not decide the comparison. A 240 MHz processor does not automatically outperform a lower-clocked MCU in every real-time or peripheral-heavy application.

STM32 versus ESP32 technical comparison of performance real-time control connectivity peripherals and development

STM32 vs ESP32 Connectivity and Peripherals: What Changes the Design?

ESP32 generally offers an advantage when Wi-Fi or Bluetooth must be integrated directly into the product, while STM32 provides a broader range of specialized embedded-control peripherals across its product families.

Feature STM32 ESP32
Wi-Fi Usually external Integrated on many variants
Bluetooth Available on selected wireless series Integrated on many variants
CAN / FDCAN Broad device support Depends on variant
Motor-control timers Strong on many series Available, but product focus differs
ADC Wide model-dependent range Integrated, variant dependent
USB Available on selected devices Available on selected variants
Ethernet Available on selected STM32 devices Usually requires external PHY and suitable variant
Wireless networking External or wireless STM32 family Core strength

STM32WB, STM32WL, and other wireless STM32 families mean it is inaccurate to say STM32 has no wireless capability. The difference is that wireless connectivity is central to the ESP32 ecosystem, while STM32 offers a broader family structure covering many embedded-control niches.

STM32 vs ESP32 Power Consumption: Which Uses Less Power?

STM32 often provides more low-power choices for battery-operated control systems, but a fair comparison depends on the exact MCU, radio state, clock configuration, and duty cycle.

Power should be evaluated under several operating conditions:

  • Active processing
  • Idle mode
  • Stop or light-sleep mode
  • Deep sleep
  • Wi-Fi active
  • Bluetooth active
  • Periodic radio wake-up
  • Bare MCU versus development board

ESP32 designs can achieve low sleep current, but wireless transmission creates short periods of much higher consumption. A sensor that wakes every few minutes, transmits data, and returns to sleep may still have excellent battery life if the duty cycle is carefully controlled.

STM32 families include devices designed specifically for low-power operation, making them attractive for metering, battery instrumentation, remote sensing, and long-life embedded devices.

For production hardware, regulator quiescent current, LEDs, USB bridges, sensors, and external radios can matter as much as the MCU specification itself.

STM32 versus ESP32 power consumption depending on sleep active and wireless transmit duty cycle

STM32 vs ESP32 Price: Which Costs Less in a Real Product?

ESP32 can have a lower total system cost when the product needs Wi-Fi or Bluetooth, while STM32 can be more economical when wireless connectivity is unnecessary.

The MCU price alone does not show the full cost. A production comparison should include:

  • MCU or module cost
  • External Wi-Fi/Bluetooth module
  • Flash and external memory
  • RF matching components
  • Antenna
  • Crystal and clock components
  • PCB area
  • Assembly cost
  • Programming and testing
  • Wireless certification requirements

An ESP32 module can combine the MCU, flash, RF circuitry, and antenna into one certified package. That can reduce design time and BOM complexity compared with adding an external wireless module to a conventional MCU.

A non-wireless STM32 design may require fewer RF-related parts and less PCB space reserved for antenna performance. The lower-cost architecture therefore depends on the final product, not the MCU unit price alone.

STM32 vs ESP32 Development: Which Is Easier to Program and Debug?

ESP32 often provides a faster learning path for connected prototypes, while STM32 offers a deeper professional embedded-development environment for projects that require detailed peripheral and hardware control.

Common STM32 tools include:

  • STM32CubeIDE
  • STM32CubeMX
  • HAL and LL libraries
  • ST-Link
  • SWD debugging
  • FreeRTOS

Common ESP32 tools include:

  • ESP-IDF
  • Arduino Core for ESP32
  • PlatformIO
  • FreeRTOS
  • JTAG debugging
  • Large open-source library ecosystem

ESP32 is popular among makers and IoT developers because Wi-Fi, Bluetooth, networking stacks, and Arduino-compatible libraries are easy to access.

STM32CubeMX can generate initialization code for clocks, GPIO, timers, ADCs, communication interfaces, and other peripherals. This can be especially useful when the application uses many hardware resources.

Arduino should not be treated as a third MCU family in this comparison. It is primarily a development platform and ecosystem that can run on different microcontroller architectures.

STM32 vs ESP32 for Robotics: Which Fits the Project Better?

STM32 is often preferred for deterministic motor and motion control, while ESP32 is attractive when the robot needs wireless communication, remote control, telemetry, or cloud connectivity.

Robotics commonly involves:

  • Motor PWM
  • Encoders
  • PID or FOC control
  • IMUs
  • Distance sensors
  • Servo control
  • Communication buses
  • Wireless control
  • Telemetry

A mobile robot with several motors and encoders may benefit from STM32 timer, DMA, ADC, and motor-control capabilities.

An ESP32 can work well for simpler robots where Wi-Fi or Bluetooth control is important. It can also manage sensors, web interfaces, telemetry, and communication with another controller.

For more demanding systems, separating responsibilities can improve architecture. One MCU can handle hard real-time control while another manages networking and user communication.

Robot using STM32 for motor control and ESP32 for wireless telemetry

STM32 vs ESP32 for Drones: Which Fits Flight Control and Connectivity?

STM32 is commonly suited to the flight-control side of a drone, while ESP32 can be useful for wireless communication and secondary connected functions.

A flight controller needs predictable handling of:

  • IMU sampling
  • Sensor fusion
  • PWM or DShot outputs
  • Control loops
  • DMA
  • Interrupt timing
  • Barometer and compass data

These requirements favor deterministic MCU behavior and strong timer/peripheral support.

ESP32 can fit other parts of the drone architecture, including Wi-Fi communication, Bluetooth setup, telemetry, configuration interfaces, and camera or peripheral control.

A simple experimental drone may run entirely on one MCU, but more advanced designs often divide time-critical control and communication functions.

Drone architecture using STM32 for flight control and ESP32 for wireless telemetry

STM32 vs ESP32 PCB Design: What Changes at Hardware Level?

STM32 and ESP32 create different PCB design priorities. STM32 designs often focus on power integrity, clocks, analog performance, programming interfaces, and peripheral routing, while ESP32 designs also need careful RF and antenna planning.

For STM32 hardware, review:

  • Decoupling capacitor placement
  • VDDA and analog grounding
  • Clock source and crystal layout
  • BOOT configuration
  • SWD programming interface
  • USB or CAN transceivers
  • External wireless modules where required

For ESP32 hardware, additional checks may include:

  • Module versus bare SoC
  • Antenna placement
  • RF keepout
  • Ground-plane geometry
  • Flash and PSRAM configuration
  • USB interface
  • Power-supply peak-current capability

Using an ESP32 module can simplify RF design, but the antenna area still needs proper PCB clearance and enclosure consideration.

At EBest Circuit, MCU placement, power integrity, RF keepout, controlled-impedance interfaces, component footprints, and PCBA requirements can be reviewed during DFM before prototype fabrication.

STM32 and ESP32 PCB design comparison showing decoupling clocks analog routing RF keepout and antenna clearance

Can STM32 and ESP32 Be Used Together?

Yes. STM32 and ESP32 are often complementary rather than direct competitors in systems that need both deterministic control and wireless connectivity.

A typical architecture might use:

STM32

  • Motor control
  • ADC sampling
  • Real-time sensors
  • Industrial communication
  • Safety-related control

UART or SPI link

ESP32

  • Wi-Fi
  • Bluetooth
  • Mobile-app communication
  • MQTT or cloud connection
  • Web configuration

This separation lets each controller handle the workload it is naturally suited to.

For example, an industrial robot may use STM32 for servo timing and encoder processing while ESP32 handles wireless diagnostics. A smart instrument can use STM32 for measurement accuracy and ESP32 for cloud connectivity.

The extra MCU adds BOM cost and firmware complexity, so this architecture is most useful when one device alone creates compromises in timing, connectivity, or certification.

STM32 vs ESP32: Which Should You Choose?

Choose according to the project requirement rather than the brand name. The most natural starting point changes with the workload.

Requirement More Natural Starting Point
Wi-Fi IoT device ESP32
Bluetooth-connected prototype ESP32
Motor control STM32
Industrial peripheral control STM32
Battery-powered control system Selected STM32 series
Wireless sensor node ESP32 or wireless STM32
High-performance real-time processing Higher-end STM32
Low-cost connected product ESP32
Wireless + deterministic control STM32 + ESP32
General maker prototype ESP32
Industrial production platform Compare exact STM32 and ESP32 variants

The final decision should consider MCU availability, software maturity, peripheral requirements, power budget, wireless needs, PCB complexity, and long-term production requirements.

A project that needs integrated Wi-Fi and rapid development may favor ESP32, while precise motor control or demanding industrial interfaces may point toward STM32. For many commercial products, comparing exact part numbers is more useful than deciding between the two families in general.

FAQ About STM32 vs ESP32

1. Is STM32 more powerful than ESP32?
It depends on the exact variants. Entry-level STM32 devices can be less powerful than some ESP32 models, while STM32H7 devices occupy a much higher embedded-performance class.

2. Is ESP32 faster than STM32F103?
In raw CPU clock and many general processing workloads, ESP32 typically has more processing headroom than STM32F103. Real-time peripheral performance still depends on the application.

3. STM32F4 vs ESP32: which is better?
STM32F4 is often attractive for real-time control, DSP, timers, and industrial peripherals. ESP32 is usually more convenient when integrated Wi-Fi or Bluetooth is a major requirement.

4. STM32H7 vs ESP32-S3: what is the main difference?
STM32H7 focuses on high-performance embedded control and processing, while ESP32-S3 combines general-purpose processing with integrated Wi-Fi and Bluetooth connectivity.

5. STM32 Blue Pill or Black Pill vs ESP32: which should beginners use?
ESP32 is often easier for wireless and IoT projects. Blue Pill and Black Pill boards are useful for learning STM32 peripherals, embedded debugging, timers, and lower-level MCU development.

6. STM32 vs ESP32 vs Arduino vs RP2040 vs Raspberry Pi: are they direct alternatives?
Not exactly. STM32, ESP32, and RP2040 are MCU platforms, Arduino is primarily a development ecosystem and board family, while most Raspberry Pi products are Linux-capable single-board computers. Raspberry Pi Pico is an MCU board based on RP2040 or newer RP-series devices.

Planning an STM32 or ESP32 PCB?

MCU selection affects more than firmware. Power architecture, clocks, RF layout, antenna clearance, analog routing, programming interfaces, connectors, and assembly requirements can all change with the selected device.

EBest Circuit supports STM32 and ESP32 PCB fabrication, DFM review, fine-pitch SMT assembly, component sourcing, programming, and functional testing. For a new embedded project, send your Gerber files, BOM, schematic, and assembly requirements to sales@bestpcbs.com for engineering review.

You may also like

PCB Transmission Line Design: Types, 50 Ohm Impedance & Rules

September 17th, 2026

A PCB transmission line is a signal trace designed together with its reference plane and dielectric so that signals travel with controlled characteristic impedance. A trace should be treated as a transmission line when its propagation delay becomes significant compared with the signal rise or fall time.

Common PCB transmission line structures include microstrip, stripline, and coplanar waveguide. Their impedance depends on trace width, copper thickness, dielectric thickness, Dk, and reference-plane geometry. For controlled-impedance designs such as 50 Ω, the final stackup should be verified with the PCB manufacturer and tested by TDR after fabrication.

PCB transmission line cross-section showing signal trace dielectric reference plane and characteristic impedance

What Is a Transmission Line on a PCB?

A PCB transmission line is a signal conductor arranged with a defined reference path so that its impedance and signal propagation can be controlled.

It normally includes:

  • A copper signal trace
  • A continuous reference plane
  • Dielectric material between signal and reference
  • Defined trace width and copper thickness
  • Controlled spacing to nearby copper
  • A predictable return-current path

At low signal speeds, a short PCB trace can often be treated as a simple connection. As signal edges become faster, voltage and current no longer appear everywhere on the trace at the same instant. The signal travels along the interconnect as an electromagnetic wave.

This is why the transmission line is not just the visible copper trace. The reference plane and dielectric are also part of the structure.

When Does a PCB Trace Become a Transmission Line?

A PCB trace should be treated as a transmission line when its propagation delay becomes significant compared with the signal rise or fall time.

Clock frequency alone is not enough to make this decision. A relatively low-frequency signal with a fast edge can still experience reflection and impedance problems.

The main factors are:

  • Signal rise and fall time
  • Trace length
  • Propagation delay
  • PCB dielectric properties

On common FR-4 structures, propagation delay is often around 150–180 ps per inch, depending on the stackup and transmission line geometry.

A useful first-pass rule is to start treating the route as a transmission line when its one-way delay approaches roughly one-sixth of the signal rise time.

So the better design question is not simply “What is the clock frequency?” but “How long does the signal take to travel through the PCB interconnect compared with its edge time?”

Short PCB trace and longer high-speed trace showing propagation delay and reflection

What Are the Main PCB Transmission Line Types?

Common The main PCB transmission line types are microstrip, embedded microstrip, stripline, and coplanar waveguide. Their main difference is how the signal trace is positioned relative to the reference plane and nearby ground copper.

Type Structure Common Use
Microstrip Outer trace over a plane RF and high-speed digital
Embedded microstrip Trace covered by dielectric Controlled outer-layer routing
Stripline Inner trace between planes High-speed internal routing
Coplanar waveguide Signal with side ground copper RF and microwave
Grounded coplanar waveguide Side ground plus lower plane RF and antenna routing

Microstrip is convenient for surface-mounted components and RF connectors. Stripline provides stronger field confinement inside the PCB. Coplanar structures are often selected when RF routing needs tighter control around the signal trace.

At EBest Circuit, transmission-line review can be included during DFM and stackup evaluation before PCB fabrication. For projects that also require PCBA, the review can extend to connector transitions, BGA breakout, component placement, and assembly constraints so that the controlled-impedance structure remains practical after the bare PCB moves into assembly.

Microstrip embedded microstrip stripline and coplanar waveguide PCB transmission line types

What Determines PCB Transmission Line Impedance?

PCB transmission line impedance is mainly controlled by trace geometry, dielectric properties, and the distance between the signal trace and its reference plane.

Important parameters include:

  • Trace width
  • Finished copper thickness
  • Dielectric thickness
  • Material Dk
  • Reference-plane position
  • Transmission line type
  • Spacing to nearby copper
  • Solder mask

For a typical microstrip, wider traces generally lower impedance, while greater distance to the reference plane tends to increase it.

This is why there is no universal trace width for 50 Ω. A 0.15 mm trace may be close to 50 Ω on one stackup but significantly different on another.

The reference plane must also remain continuous. Plane splits, large voids, and abrupt reference changes can disturb the electromagnetic field even when trace width remains unchanged.

How Do You Design a 50 Ohm Transmission Line on a PCB?

A 50 ohm PCB transmission line is designed by matching trace geometry to the actual PCB stackup until the calculated characteristic impedance reaches approximately 50 Ω.

The design should start with:

  • Signal layer
  • Reference plane
  • Material type
  • Dielectric thickness
  • Finished copper thickness
  • Target impedance
  • Impedance tolerance

There is no fixed 50 Ω trace width that works for every PCB.

A practical design process is:

  1. Define the 50 Ω target.
  2. Confirm the PCB stackup.
  3. Select microstrip, stripline, or another structure.
  4. Calculate the initial trace dimensions.
  5. Verify the cross-section with a field solver.
  6. Apply manufacturing compensation if required.
  7. Fabricate an impedance coupon.
  8. Verify the finished result with TDR.

50 Ω is widely used because many RF cables, connectors, instruments, amplifiers, filters, and antennas are designed around the same impedance environment.

How Is PCB Transmission Line Impedance Calculated?

A PCB transmission line calculation can be estimated with analytical formulas, online calculators, or electromagnetic field solvers.

Analytical formulas are useful for understanding how trace width, dielectric thickness, copper thickness, and Dk affect impedance.

A PCB transmission line impedance calculator is useful for early estimates, but the result should be checked against the final production stackup.

Online PCB transmission line calculators are convenient for early layout. Typical inputs include:

  • Trace width
  • Copper thickness
  • Dielectric thickness
  • Dielectric constant
  • Ground spacing

Different calculators may produce slightly different values because they use different equations and assumptions.

For final controlled-impedance production, a 2D field solver is usually more reliable because it can model the actual PCB cross-section, including conductor shape, dielectric regions, solder mask, and coplanar spacing.

50 ohm PCB transmission line calculation with trace width dielectric thickness copper thickness and field solver

What PCB Layout Rules Keep Transmission Line Impedance Stable?

Good PCB transmission line layout design keeps the routing geometry and return path consistent along the signal route.

Key layout rules include:

  • Route over a continuous reference plane.
  • Avoid unnecessary trace-width changes.
  • Keep neck-down sections short.
  • Minimize unnecessary vias.
  • Provide a return path during layer changes.
  • Control spacing to nearby traces and copper.
  • Avoid long via stubs on very high-speed signals.

A signal via changes the local transmission structure, so its pad, antipad, barrel, and stub can affect high-speed performance.

Connectors, pads, vias, and package breakouts should also be treated as part of the channel. A well-controlled 50 Ω trace can still experience reflections if these transitions create large impedance discontinuities.

PCB controlled impedance routing over continuous reference plane with via transition and plane split comparison

How Is PCB Transmission Line Impedance Controlled and Tested in Manufacturing?

PCB manufacturers control transmission line impedance by matching the electrical target to the actual production stackup, compensating the artwork when necessary, and verifying the finished structure with TDR.

Before fabrication, the manufacturer normally reviews:

  • Material grade and Dk
  • Dielectric thickness
  • Finished copper thickness
  • Trace width and spacing
  • Target impedance
  • Required tolerance

Production artwork may be adjusted slightly because plating and etching change the finished conductor geometry.

For controlled-impedance boards, an impedance coupon is usually fabricated on the same panel. TDR testing then checks whether the finished structure meets the specified impedance.

Common requirements include:

  • 50 Ω ±10%
  • 90 Ω differential ±10%
  • 100 Ω differential ±10%

For quotation and stackup review, provide the Gerber or ODB++ files, material requirement, copper weight, target impedance, routing layer, and tolerance.

Technician performing TDR impedance testing on PCB impedance coupon

FAQ About PCB Transmission Lines

1. Is every PCB trace a transmission line? Technically yes, but transmission line analysis is normally needed only when trace delay becomes significant compared with the signal rise or fall time.

2. Why is 50 ohms commonly used for PCB transmission lines? Because many RF cables, connectors, instruments, antennas, and components are designed around a 50 Ω system.

3. What is the difference between microstrip and stripline? Microstrip runs on an outer PCB layer above a reference plane. Stripline runs inside the PCB between reference planes.

4. Does PCB trace length change characteristic impedance? No. Characteristic impedance is mainly determined by geometry and dielectric properties. Length mainly affects propagation delay, loss, and phase.

5. Can FR-4 be used for a 50 ohm transmission line? Yes. FR-4 is suitable for many 50 Ω designs, although lower-loss laminates may be preferable at higher frequencies or where insertion loss is tightly controlled.

6. How is PCB transmission line impedance measured? It is commonly verified with TDR using an impedance coupon fabricated with the production panel.

Ready to Review Your PCB Transmission Line Design?

A transmission line that calculates as 50 Ω may shift after the final dielectric thickness, copper plating, and etching process are defined. Reviewing the production stackup before fabrication helps reduce impedance deviation and avoid unnecessary revisions.

EBest Circuit supports controlled-impedance PCB manufacturing and PCBA for high-speed digital, RF, microwave, HDI, Rogers, hybrid-material, and low-loss multilayer projects. If you have similar projects, you are welcome to send your Gerber files and detailed PCB specifications to sales@bestpcbs.com for stackup and DFM review.
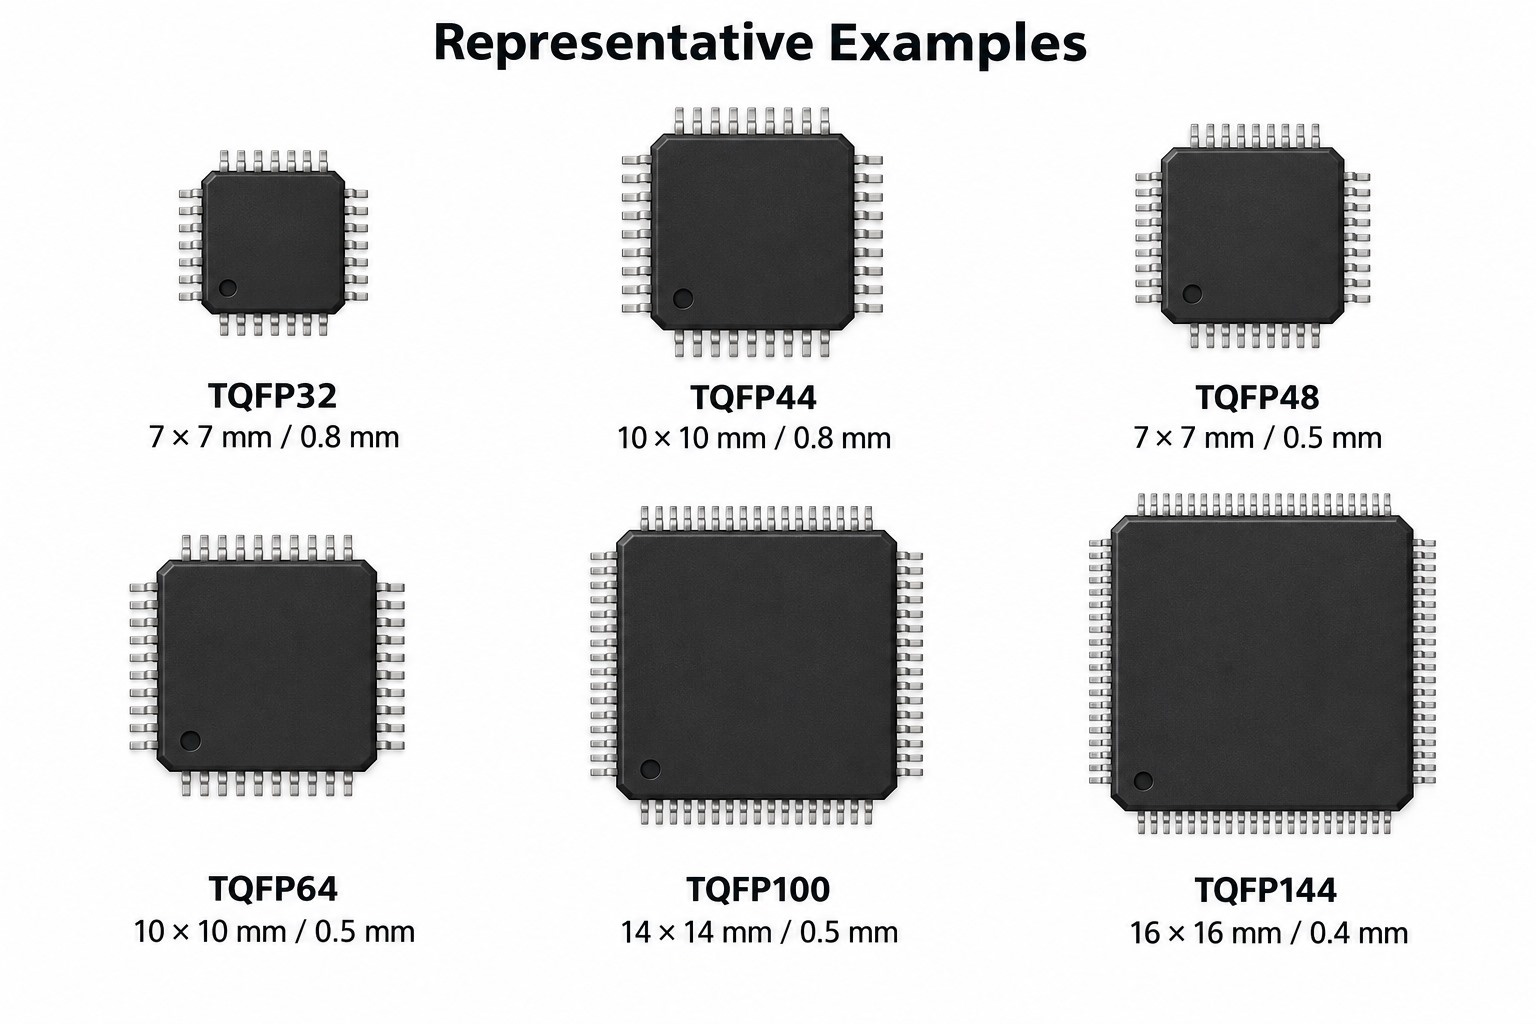
You may also like

HVLP Copper Foil for AI Server PCBs: M9, 52-Layer Designs & Signal Loss

September 17th, 2026

AI server PCB materials are entering another upgrade cycle. A September 16, 2026 industry report highlighted movement toward 52-layer PCB architectures and M9-class CCL as cloud providers continue expanding AI infrastructure. The change is not simply more copper layers; higher data rates are forcing designers to control dielectric loss, conductor loss, impedance consistency, and phase behavior together.

That is why HVLP copper foil is becoming more important. As resin and glass systems reduce dielectric loss, rough copper can consume a larger portion of the channel-loss budget. The practical question for PCB engineers is therefore no longer only “Which laminate grade should I use?” but also which copper profile is needed, on which layers, and how should that low roughness be preserved through fabrication?

HVLP copper foil for AI server PCBs with M9 materials and 52-layer high-speed design

Key Takeaways

  • HVLP copper foil is used to reduce conductor loss in high-speed PCB channels by lowering the surface profile at the copper-dielectric interface.
  • AI server PCBs are moving toward higher layer counts and lower-loss M9-class material systems, making copper roughness increasingly important alongside resin Df and glass construction.
  • HVLP describes copper surface profile, not copper thickness. An 18 μm or 35 μm foil can still be a low-profile copper construction.
  • A 52-layer PCB does not necessarily require HVLP on every layer. Long high-speed signal channels usually deserve the lowest-profile copper first.
  • HVLP3, HVLP4, and HVLP5 are not universal IPC roughness classes. Engineers should verify actual Rz/Rq, foil thickness, treatment side, peel strength, and insertion-loss data.
  • Very smooth copper creates a manufacturing trade-off: lower conductor loss must be balanced with sufficient copper-to-resin adhesion.
  • PCB processing also matters. Aggressive inner-layer pretreatment can increase roughness and reduce the signal-integrity advantage of the incoming HVLP foil.

Why Is HVLP Copper Foil Demand Rising in AI Server PCBs?

HVLP copper foil demand is rising because AI server boards are combining more PCB layers with faster, longer loss-sensitive channels. The current AI infrastructure cycle is pushing higher-layer-count architectures together with M9-class material upgrades.

Three changes are happening at the same time:

  • PCB layer counts are increasing.
  • SerDes data rates continue moving toward 112G and 224G-class links.
  • CCL systems are reducing dielectric loss, making conductor loss more visible.

The demand increase therefore comes from both more high-speed PCB material per server and a higher proportion of signal layers requiring smoother copper.

What Is HVLP Copper Foil?

HVLP copper foil is a very-low-profile copper construction designed to maintain a smoother copper-dielectric interface than conventional electrodeposited copper.

The exact terminology varies by supplier. Some suppliers describe HVLP as ultra-low-profile copper, while the industry also uses “hyper very low profile” informally. What matters electrically is the actual surface morphology and measured roughness rather than the name alone.

Typical parameters to review include:

  • Rz surface roughness
  • Ra, Rq, or Sq where specified
  • Treatment-side roughness
  • Foil thickness
  • Tensile strength
  • Elongation
  • Peel strength

Copper profile and copper thickness are different parameters. A smoother HVLP foil can still be supplied in common thicknesses such as 12, 18, or 35 μm.

HVLP copper foil smooth surface compared with rough standard copper foil

HVLP vs VLP vs RTF vs Standard Copper Foil: What Changes?

The main difference is the surface profile presented to the dielectric. Lower-profile foil reduces the microscopic path length seen by high-frequency surface current.

Copper Foil Type Surface Character Typical Design Direction
Standard ED Relatively rough General-purpose PCB
RTF Reduced profile on functional side Mid- to high-speed PCB
VLP Low profile High-speed digital / RF
HVLP Very low profile Very-high-speed low-loss channels
Advanced HVLP Extremely low profile 112G/224G, AI server, mmWave-class applications

These categories should not be treated as fixed global roughness ranges. Supplier processes, treatment methods, and naming conventions differ. For design work, the grade name should therefore be followed by the actual roughness specification and measured electrical performance.

HVLP VLP RTF and standard ED copper foil surface roughness comparison

Why Does M9-Class CCL Still Need Smoother Copper Foil?

M9-class material reduces dielectric loss, but total channel loss also includes conductor loss. Improving only the resin and glass system does not eliminate loss caused by rough copper.

Material Element Main Role
Low-loss resin Reduces dielectric loss
Low-Dk / advanced glass Improves dielectric behavior and dimensional control
HVLP copper foil Reduces conductor and insertion loss
Complete low-loss CCL Balances all three for the required channel target

At lower frequencies, dielectric loss may dominate enough that moderate copper roughness is acceptable. As signaling frequency rises, however, current becomes increasingly concentrated near the conductor surface.

That makes the microscopic copper profile part of the signal path. A very-low-Df resin paired with unnecessarily rough copper can therefore surrender part of the improvement gained from the dielectric system. M9 should be evaluated as a complete laminate system rather than as a resin grade alone.

M9-class CCL structure with low-loss resin advanced glass and HVLP copper foil

How Does Copper Roughness Increase Conductor and Insertion Loss?

At high frequency, current flows primarily near the copper surface because of skin effect. When that surface is rough, the current follows a more complex microscopic path and experiences higher effective resistance.

The practical effects can include:

  • Higher conductor loss
  • Higher insertion loss
  • Apparent changes in effective Dk
  • Additional phase variation
  • Greater channel-to-channel variation

Published test data has shown that copper profile alone can materially change insertion loss even when the dielectric material remains the same. The exact dB/in change depends on substrate, trace geometry, frequency, and foil construction, so loss figures should always be tied to the actual test vehicle.

Smooth copper versus rough copper showing lower and higher insertion loss

Why Do 52-Layer AI Server PCBs Increase HVLP Copper Foil Demand?

Higher layer counts increase HVLP demand through both a quantity effect and a material-mix effect.

Quantity effect

  • More copper foil
  • More CCL cores
  • More prepreg
  • More signal-layer area
  • More lamination materials

Mix effect

At the same time, more routing may move from conventional foil or older low-profile grades toward lower-profile constructions as channel loss budgets tighten.

However, a 52-layer PCB does not mean all 52 layers use HVLP copper foil. Ground planes, power planes, short control traces, and lower-speed auxiliary layers may use different copper constructions.

52-layer AI server PCB showing quantity effect and mix effect on HVLP copper foil demand

Which PCB Layers Actually Need HVLP Copper Foil?

HVLP should normally be prioritized according to channel-loss sensitivity rather than applied to every copper layer by default.

Typical candidates include:

  • Long SerDes routing
  • 112G/224G-class channels
  • PCIe and other high-speed differential links
  • Switch and accelerator interconnects
  • Backplane or midplane routing
  • Loss-sensitive memory/network interfaces
  • High-frequency RF or mmWave layers where applicable

Layers that may not require the same profile include:

  • Power planes
  • Ground planes
  • Short GPIO routes
  • Low-speed management buses
  • Short local control connections

The actual choice depends on trace length, data rate, dielectric thickness, insertion-loss budget, and laminate system.

AI server PCB layer stack highlighting high-speed layers that should prioritize HVLP copper foil

HVLP3 vs HVLP4 vs HVLP5: How Should Engineers Interpret the Grades?

HVLP3, HVLP4, and HVLP5 generally indicate progressively smoother copper within a supplier’s product family, but these labels are not universal IPC roughness classifications.

When comparing grades, engineers should request:

  • Rz
  • Ra / Rq / Sq where available
  • Treatment-side roughness
  • Copper thickness
  • Treatment chemistry
  • Peel strength
  • Resin compatibility
  • Insertion-loss test data

A buyer should therefore avoid specifying only “HVLP4 required.” A better requirement links the foil grade to a named laminate construction, roughness target, and electrical loss objective.

What Manufacturing Challenges Come with HVLP Copper Foil?

The manufacturing challenge with HVLP is to keep the copper surface smooth enough for low loss while maintaining enough adhesion to survive lamination, thermal cycling, and assembly.

Important controls include:

  • Copper-to-resin bonding
  • Inner-layer pretreatment
  • Brown oxide or alternative oxide chemistry
  • Lamination pressure and temperature
  • Resin compatibility
  • Etching compensation
  • Peel strength
  • Impedance consistency
  • Layer registration
  • High-layer-count warpage

PCB processing can change the incoming copper surface. The relevant question is not only “Was HVLP purchased?” but also “What roughness remains at the finished signal interface after fabrication?”

HVLP copper foil manufacturing process and engineering specification checklist

How Should Engineers Specify and Verify HVLP Copper Foil?

An HVLP requirement should connect the material specification to the actual electrical channel requirement.

For quotation or stackup review, provide:

  • Target data rate
  • Operating or Nyquist frequency
  • PCB layer count
  • Laminate family
  • Copper foil supplier and grade, if mandatory
  • Copper thickness
  • Required Rz / Rq / Sq
  • Treatment side
  • Layers requiring HVLP
  • Impedance tolerance
  • Maximum insertion loss
  • Critical trace length
  • Peel-strength requirement
  • Thermal and reliability requirements

Verification may include:

  • Impedance coupons
  • TDR
  • Insertion-loss coupons
  • VNA / S-parameter testing
  • Material certificate or COC
  • Lot traceability

For very-high-speed projects, the laminate, glass style, copper foil, stackup geometry, and fabrication treatment should be qualified together rather than approved as independent specifications.

What Cost and Supply Risks Should Buyers Check for HVLP4 and HVLP5?

Higher-grade HVLP introduces both material-cost and supply-chain risk because qualification is more restrictive than for standard copper foil.

When selecting an HVLP copper foil supplier, compare the actual Rz/Rq limits, treatment method, laminate qualification, and measured channel-loss data rather than relying on the grade name alone.

Buyers should check:

  • Qualified copper-foil suppliers
  • Qualified CCL combinations
  • Minimum order quantities
  • Lead time
  • Alternative material approval
  • Lot-to-lot roughness control
  • Qualification quantities
  • Insertion-loss validation
  • Whether substitutions require customer approval

A lower-cost foil with the same “HVLP4” label should not automatically be treated as electrically or mechanically equivalent. The actual laminate system, surface treatment, roughness, adhesion, and measured channel loss still need qualification.

FAQ About HVLP Copper Foil

1. What does HVLP mean in copper foil?
HVLP refers to very-low-profile copper foil developed for lower conductor loss. Supplier terminology varies, so the actual Rz/Rq and product specification are more important than the acronym alone.

2. Is HVLP copper thinner than standard copper foil?
No. Copper thickness and copper surface profile are separate parameters. HVLP can be supplied in common foil thicknesses such as 12, 18, or 35 μm.

3. What is the difference between VLP and HVLP copper foil?
Both reduce copper surface roughness, but HVLP generally targets a lower surface profile and more demanding high-speed channels. Exact roughness limits depend on the supplier.

4. Does M9 CCL always use HVLP5 copper foil?
No. M9-class material systems vary by laminate supplier and application. The required copper profile depends on data rate, stackup, trace length, insertion-loss target, and qualified material construction.

5. Does every signal layer need HVLP copper foil?
No. HVLP is normally prioritized for the most loss-sensitive signal layers. Short low-speed routes and non-signal planes may use other copper constructions.

6. What roughness value should I specify for a high-speed PCB?
There is no universal Rz value for every high-speed design. The correct target should be derived from the channel-loss budget and verified against the actual foil, laminate, stackup, and fabrication process.

Planning a High-Speed PCB with HVLP Copper Foil?

HVLP selection is only one part of a high-speed material system. Laminate Dk/Df, glass style, copper profile, trace geometry, layer assignment, impedance, inner-layer treatment, and insertion-loss testing all need to work together.

EBest Circuit can review stackup requirements, impedance targets, copper thickness, laminate availability, HVLP requirements, and manufacturability before quotation. For advanced low-loss PCB projects, send your Gerber files, stackup, material requirement, target impedance, and loss specification to sales@bestpcbs.com for engineering review.
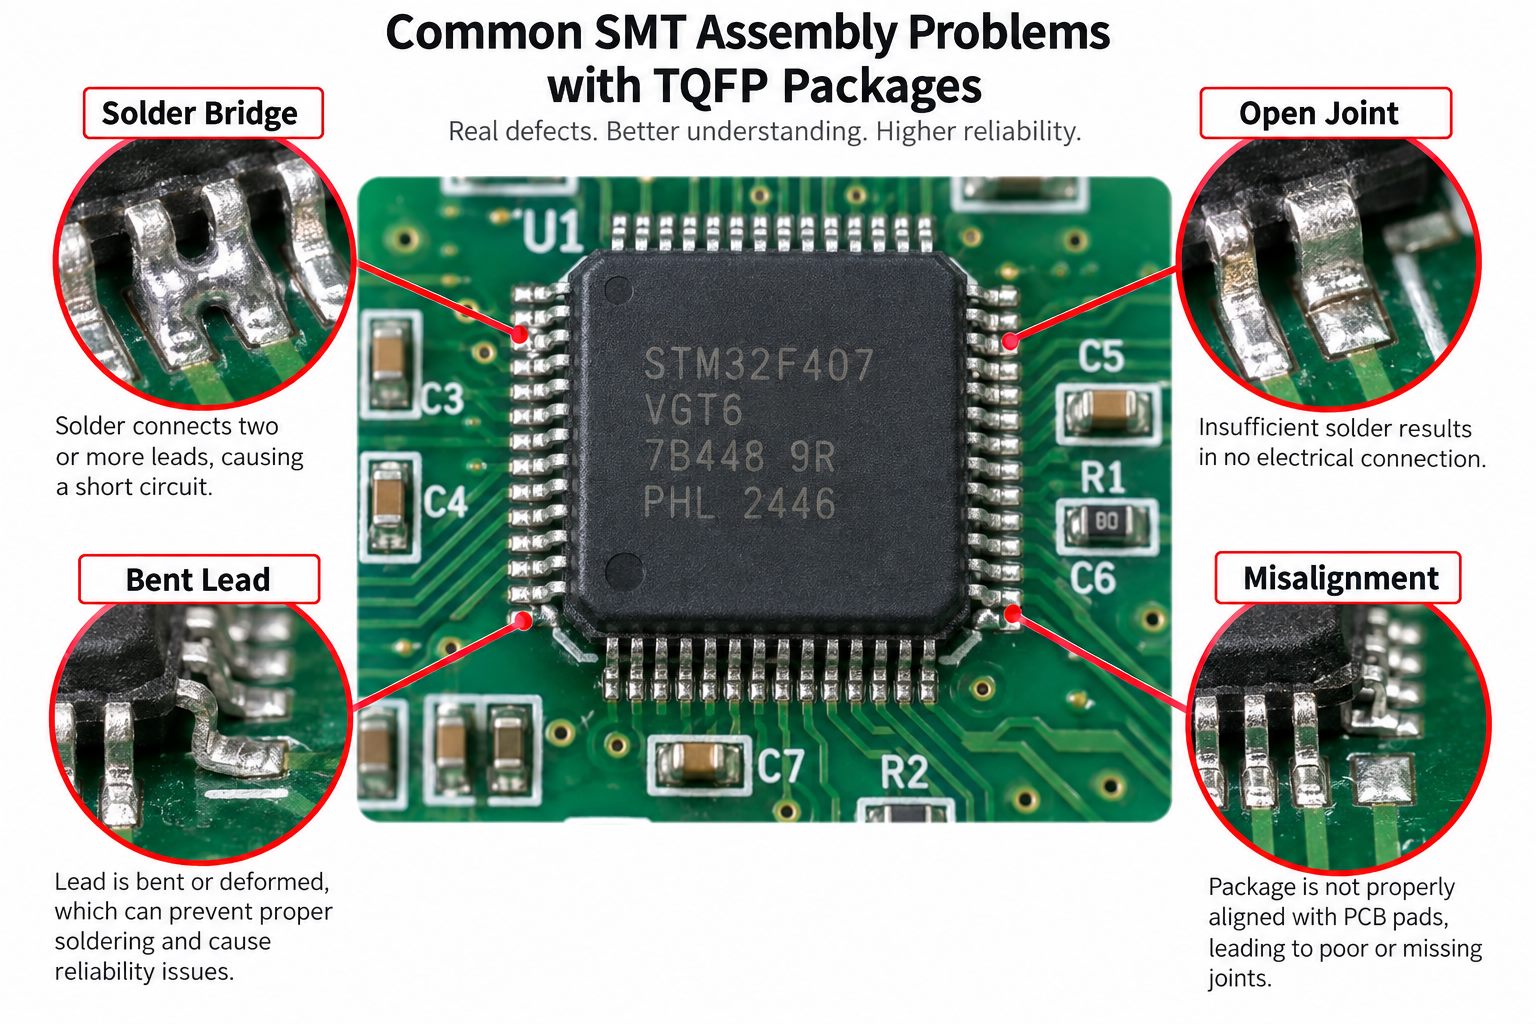
You may also like

Breakout Boards: Meaning, Types, Uses & PCB Design Guide

September 17th, 2026

A breakout board is a small PCB that takes difficult-to-access pins from an IC, sensor, module, or connector and routes them to larger pads, headers, or terminals. This makes fine-pitch or compact components much easier to prototype, test, and connect without designing a complete custom PCB first.

Breakout boards are widely used with Arduino, ESP32, sensors, USB-C, RJ45, SMD packages, and power connectors. Some simply expose pins, while others add regulators, pull-up resistors, level shifting, ESD protection, or signal conditioning. Understanding that difference matters when selecting or designing a board.

Breakout boards including sensor USB-C RJ45 terminal SMD adapter and ESP32 boards

What Is a Breakout Board?

A breakout board is a small printed circuit board that converts a difficult component interface into a connection that is easier to access. For example, a QFN sensor may have pads spaced too closely for jumper wires or a breadboard, so the breakout PCB routes those pads outward.

Common connection formats include:

  • 2.54 mm pin headers
  • Screw terminals
  • Test pads
  • Edge connectors
  • Larger solder pads

The same principle applies to connectors. A USB-C or RJ45 breakout board exposes individual connector contacts so they can be reached during prototyping, testing, or wiring.

Breakout boards usually perform one focused task. They are not necessarily complete development platforms and may contain no processor, firmware, or programmable circuitry.

Fine-pitch IC mounted on a breakout board with accessible header pins

How Does a Breakout Board Work?

A breakout board routes closely spaced component or connector pins through PCB copper traces to larger, easier-to-use connection points. The basic signal path is:

Component or connector → PCB fan-out traces → accessible pads or headers

A typical breakout board may contain:

  • The main IC, sensor, module, or connector
  • Copper fan-out routing
  • Pin headers or terminal blocks
  • Ground and power connections
  • Decoupling capacitors
  • Optional supporting components

On a passive board, the traces may connect almost directly from the device pins to the headers. An active breakout can add functions such as voltage regulation or level shifting, allowing a low-voltage sensor to interface safely with a 3.3 V or 5 V controller.

The PCB can also simplify pin identification. Silkscreen labels such as VCC, GND, SDA, SCL, TX, RX, D+ and D- help reduce wiring errors during prototyping.

What Are the Main Types of Breakout Boards?

Breakout boards are usually classified by the component or interface they make easier to access.

Breakout Board Type What It Exposes Common Examples
SMD / IC breakout Fine-pitch package pins QFN, DFN, SOIC, TSSOP
Sensor breakout Sensor power and I/O IMU, pressure, temperature
MCU / module breakout GPIO and communication pins ESP32 modules
Connector breakout Connector contacts USB-C, USB, RJ45
Power breakout Power supply rails ATX connectors
Communication breakout Bus or transceiver signals CAN, RS485, UART

SMD breakout boards help when a surface-mount package cannot plug directly into a breadboard, while sensor breakout boards may add decoupling, pull-ups, or voltage support around the sensor.

Connector breakout boards expose contacts through headers, pads, or screw terminals. Power breakout boards separate supply rails into accessible connection points for prototyping or test setups.

At EBest Circuit, custom breakout board projects can be reviewed together with the component footprint, connector layout, BOM, assembly process, and test requirements before prototype fabrication.

Passive vs Active Breakout Boards: What Is the Difference?

A passive breakout board mainly reroutes electrical connections, while an active breakout board adds circuitry that changes, protects, or conditions the signal or power.

A passive breakout board may contain only:

  • Copper traces
  • Pads
  • Headers
  • Connectors
  • Screw terminals

Typical examples include an RJ45-to-terminal adapter or a QFN-to-DIP adapter. An active breakout board may add:

  • Voltage regulators
  • Pull-up or pull-down resistors
  • Logic-level shifters
  • ESD protection
  • Filters
  • Transceivers
  • Oscillators
  • Signal-conditioning ICs

Two boards using the same connector can therefore behave very differently. A passive USB-C breakout may only expose connector pins, while another design may include CC resistors, a power controller, or a USB interface IC.

Before connecting a breakout board, check its schematic or pinout rather than assuming every pin is routed directly from the original device.

Passive and active breakout board comparison

How Are Breakout Boards Used with Arduino and ESP32?

Breakout boards make it easier to connect sensors, interfaces, and modules to Arduino or ESP32 development boards without creating a custom PCB first.

A breakout board for ESP32 can fan out compact module pins to standard headers, labeled GPIO connections, or terminal blocks for faster bench testing.

Common connections include:

  • GPIO
  • I²C
  • SPI
  • UART
  • PWM
  • Analog signals
  • Power and ground

A sensor breakout may expose VCC, GND, SDA, and SCL, allowing it to connect directly to an Arduino or ESP32 through I²C. An ESP32 breakout board may instead route the module’s closely spaced pins to standard headers, terminal blocks, or clearly labeled GPIO connections.

Voltage compatibility still needs to be checked because ESP32 GPIO typically operates at 3.3 V, while some Arduino boards use 5 V logic. Also confirm whether the breakout already includes pull-ups, voltage regulation, USB-to-UART circuitry, EN or BOOT controls, or level shifting.

Breakout boards connected to Arduino and ESP32 development boards

What Should You Check on USB-C, RJ45 and Screw-Terminal Breakout Boards?

Connector breakout boards should be selected by electrical capability, not just connector shape.

For USB-C breakout boards, check:

  • Which of the 24 USB-C pins are exposed
  • Whether CC1 and CC2 are available
  • Whether CC resistors are installed
  • USB 2.0 or higher-speed data support
  • Differential-pair routing
  • Current rating
  • Whether USB Power Delivery circuitry is included

A USB-C receptacle does not automatically mean the board supports Power Delivery or high-speed USB. For RJ45 breakout boards, check whether the board simply exposes all eight contacts or also includes magnetics, LEDs, shielding, or Ethernet-specific circuitry.

For screw-terminal breakout boards, check:

  • Terminal pitch
  • Wire gauge
  • Current rating
  • Voltage rating
  • Connector pin mapping

Breakout Board vs Breadboard vs Development Board: What Is the Difference?

A breakout board, breadboard, and development board all support prototyping, but they solve different problems.

Feature Breakout Board Breadboard Development Board
Main purpose Expose component pins Build temporary circuits Run and program a controller
Is it a PCB? Yes Usually no Yes
Usually programmable? No No Yes
Contains target IC? Often Not by itself Yes
Typical use Component evaluation Wiring experiments Firmware and system development

A breadboard provides reusable connection points for temporary circuits, while a breakout board adapts a specific component or connector into a more convenient electrical interface.

A development board normally contains a programmable MCU or processor plus support circuitry such as USB, clocks, memory, voltage regulation, and programming interfaces. Arduino and ESP32 development boards fit this category; a separate sensor or connector PCB attached to them is usually the breakout board.

Breakout board breadboard and development board comparison

What Matters When Designing a Custom Breakout Board PCB?

A custom breakout board should make the target component easier to use without creating new electrical, mechanical, or assembly problems.

A breakout board PCB design should preserve the component pinout while making power, signals, mounting, and test access easier to verify.

Important PCB design checks include:

  • Correct component footprint
  • Header or terminal pitch
  • Pin numbering and silkscreen labels
  • Fan-out routing from fine-pitch packages
  • Power and ground routing
  • Decoupling capacitor placement
  • Ground-plane continuity
  • Test points
  • Mounting holes
  • Connector mechanical support

Active breakout boards may also need voltage regulation, level shifting, ESD protection, filtering, pull-up resistors, or signal conditioning.

High-speed interfaces need tighter PCB control. USB, Ethernet-related signals, RF modules, and fast differential buses may require controlled impedance, matched differential pairs, short stubs, and continuous return paths.

Very small QFN, DFN, or BGA packages can also affect manufacturability. They may require tighter solder-mask alignment, via-in-pad structures, or X-ray inspection after assembly.

EBest Circuit can review breakout-board Gerber files, BOMs, connector footprints, stackups, fine-pitch packages, and PCBA requirements during DFM before prototype fabrication.

Custom breakout board PCB design showing footprint fan-out power routing test points and mounting holes

When Should You Replace a Breakout Board with a Custom PCB?

A breakout board is useful during evaluation, but a custom PCB usually becomes more practical once the circuit architecture is stable.

Consider moving to a custom PCB when:

  • The prototype has been electrically validated.
  • Several breakout boards are connected together.
  • Product size must be reduced.
  • Connectors need fixed mechanical positioning.
  • Production quantity is increasing.
  • Assembly time is becoming expensive.
  • Signal integrity or EMC performance matters.
  • Power distribution needs tighter control.
  • BOM cost needs to be reduced.
  • Repeated manual wiring is creating errors.

A custom PCB can combine the validated functions into one layout with fixed connector positions, shorter interconnects, defined mounting, and repeatable assembly.

Prototype using breakout boards transitioning to a custom PCB

FAQ About Breakout Boards

1. Is a breakout board the same as a PCB?
A breakout board is a type of PCB. It is usually designed around one component, module, connector, or interface rather than a complete product circuit.

2. What does breakout board mean?
It means a board that “breaks out” difficult-to-access electrical pins into larger, easier connection points such as headers, pads, or terminals.

3. Is an SMD adapter a breakout board?
Yes. Many SMD adapters are breakout boards because they convert fine-pitch SMD pins into breadboard-friendly or through-hole connections.

4. Can one breakout board work with both Arduino and ESP32?
Sometimes. The pin interface may be compatible, but voltage levels, power requirements, and communication settings must also match.

5. Can breakout boards be used in production products?
Yes, but they are more commonly used for prototyping, testing, and low-volume systems. A custom PCB is usually more compact and economical for larger production runs.

6. Do USB-C breakout boards support Power Delivery?
Not necessarily. A basic USB-C breakout may only expose connector pins. USB Power Delivery requires the appropriate CC and PD controller circuitry.

Ready to Turn a Breakout Board Prototype into a Custom PCB?

Breakout boards are effective for proving a circuit quickly, but production hardware usually needs a more integrated layout with controlled power, fixed connectors, shorter interconnects, and repeatable assembly.

EBest Circuit supports custom PCB fabrication, fine-pitch component assembly, connector assembly, DFM review, and prototype-to-production PCBA. If your prototype is moving beyond breakout boards, send your Gerber files, BOM, schematics, and assembly requirements to sales@bestpcbs.com for engineering review.
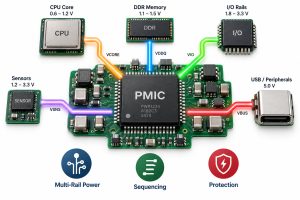
You may also like