PCB manufacturing PCB manufacturing
Home > Blog

HDI PCB Stackup

22-Layer HDI PCB Design & Manufacturing: Stackup, Vias & Impedance
Thursday, November 12th, 2026

An 22-layer HDI PCB must accommodate dense BGA routing, high-speed signals, complex buried vias, and multiple power planes within strict manufacturing limits. When a design requires 0.10 mm microvias, deep buried vias, ±10% impedance tolerance, and a fixed board thickness, can these requirements be achieved without changing the original layout?

Possibly, but not on assumption alone. The proposed stackup, via spans, material constructions, and finished trace geometry must be checked together before an unchanged layout can be approved for fabrication.

EBest Circuit provides multilayer PCB manufacturing, HDI fabrication, and DFM review for complex electronic projects. We help customers evaluate stackup construction, interconnection reliability, material compatibility, and manufacturing feasibility before prototyping and production.
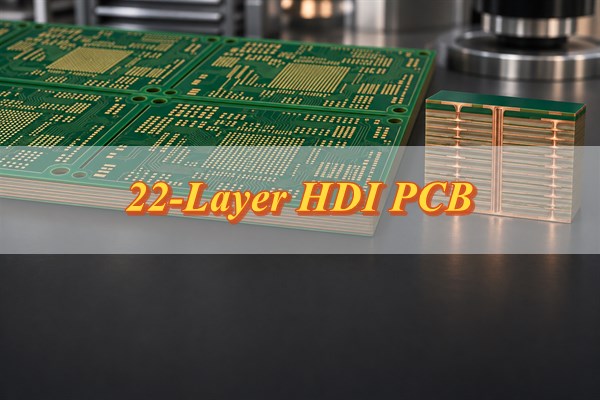
22-Layer HDI PCB, https://www.bestpcbs.com/blog/2026/11/22-layer-hdi-pcb/

What Is a 22-Layer HDI PCB, and Where Is It Used?

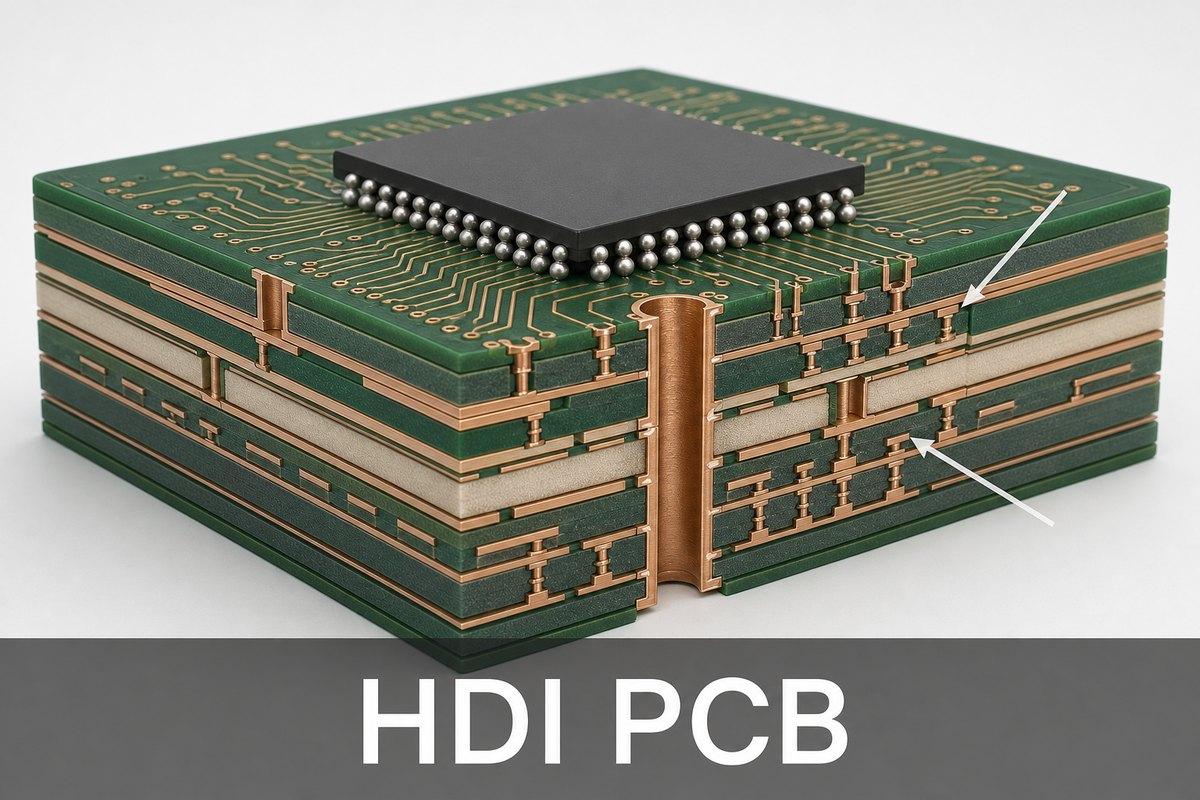
An 22-layer HDI PCB contains 22 conductive copper layers with high-density interconnections such as laser microvias, blind vias, buried vias, and via-in-pad structures. It provides additional routing capacity for high-pin-count components while reducing the space occupied by conventional through-hole connections.

Typical applications include:

  • High-speed computing and FPGA boards: High-pin-count BGAs, DDR memory, SerDes interfaces, and multiple power domains.
  • Networking and telecommunications: Switches, routers, and communication equipment requiring controlled impedance and low-loss transmission.
  • Industrial VME systems: Processor cards with fixed mechanical dimensions, backplane connectors, and high-density routing.
  • Medical instrumentation: High-channel-count signal acquisition, imaging, and processing equipment.
  • Aerospace electronics: Compact control and communication hardware with project-specific reliability requirements.

Not every 22-layer PCB requires HDI construction. Conventional multilayer fabrication may be sufficient when through-holes provide adequate routing space. HDI becomes more appropriate when BGA fanout, routing density, or signal transitions cannot be accommodated efficiently using conventional vias.

What Does a 22-Layer HDI PCB Stackup Look Like?

A 22-layer HDI PCB stackup distributes high-speed signal layers, ground planes, and power planes across 22 copper layers. Critical signal layers should be positioned next to suitable reference planes to support controlled impedance and continuous return-current paths.
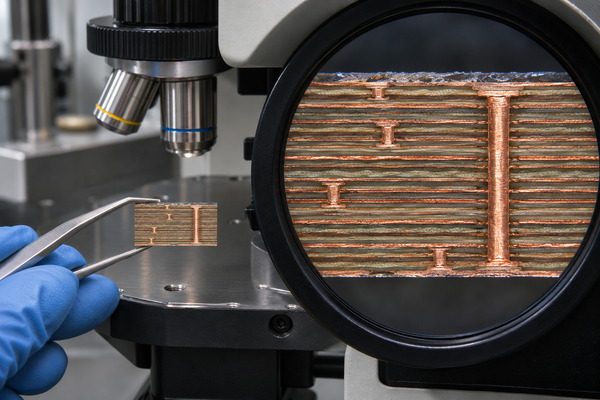
22-Layer HDI PCB, https://www.bestpcbs.com/blog/2026/11/22-layer-hdi-pcb/

The following is an example of a symmetrical functional layer arrangement.

Layer Pair Layer Function
L1 / L22 Outer signal and BGA breakout
L2 / L21 Ground reference
L3 / L20 High-speed signal
L4 / L19 Ground reference
L5 / L18 Internal signal
L6 / L17 Power distribution
L7 / L16 Ground reference
L8 / L15 Internal signal
L9 / L14 Ground reference
L10 / L13 High-speed signal
L11 / L12 Central ground reference

L3 and L20 can carry controlled-impedance stripline signals, while L10 and L13 provide additional high-speed routing channels. The remaining signal layers accommodate BGA fanout and internal connections.

A production-ready stackup also requires:

  • Core and prepreg materials: Actual material constructions and dielectric properties.
  • Dielectric thickness: Individual spacing between copper layers.
  • Copper thickness: Finished copper weights for signal and power layers.
  • Impedance calculations: Trace geometry and reference-plane relationships for each controlled layer.
  • Lamination balance: Suitable copper distribution and mechanical stability.

For a 2.25 mm nominal finished thickness, the complete copper and dielectric construction must fit the approved mechanical requirements. Dielectric spacing cannot be adjusted independently because it also affects impedance and drilling geometry.

How Do 1+20+1 HDI Structures Support Complex Layer Interconnections?

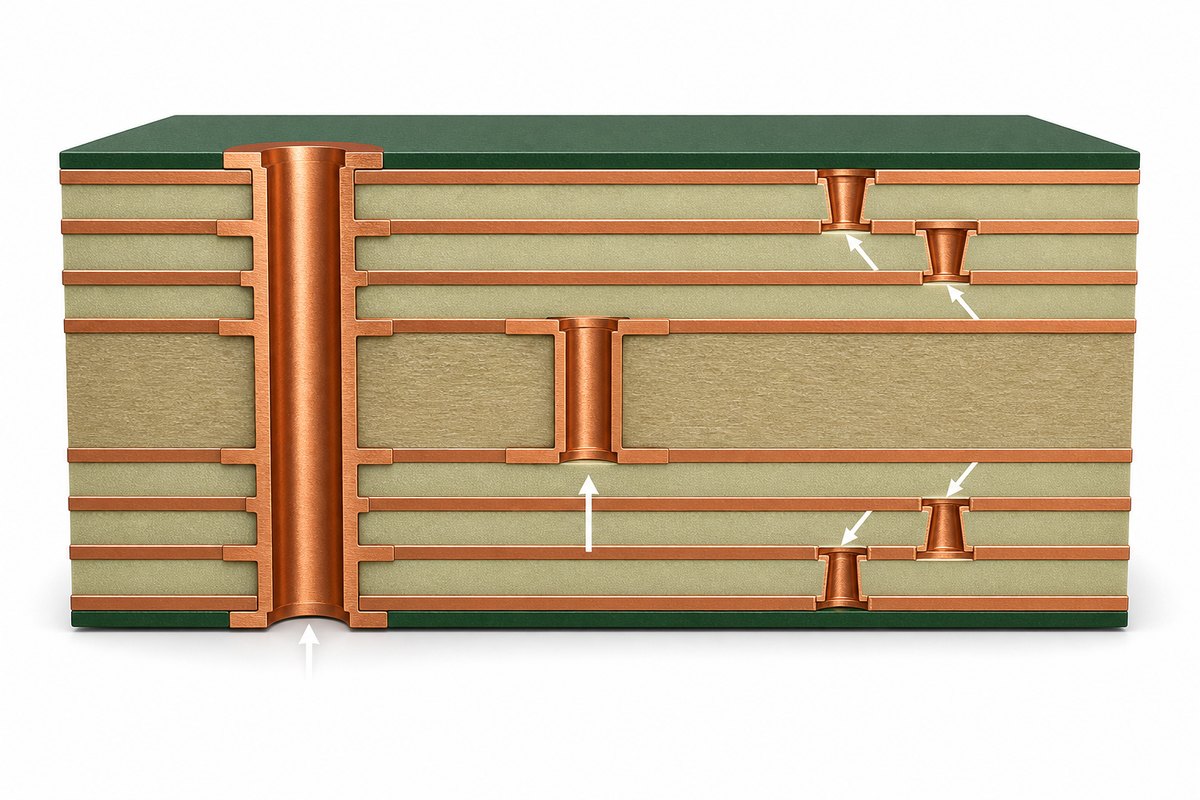
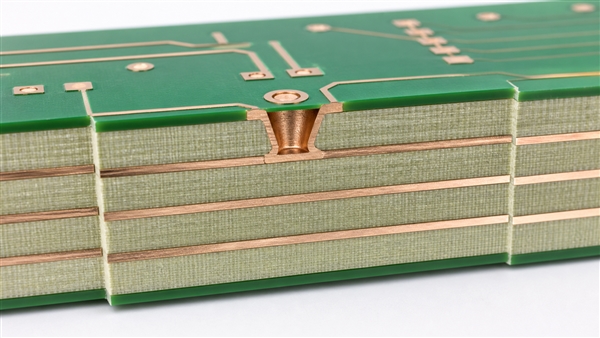
A 22-layer 1+20+1 HDI PCB consists of a 20-layer central structure with one HDI buildup layer on each side. Outer microvias provide compact surface connections, while buried vias and through-holes connect the required internal layers.

The main interconnections include:

  • L1–L2 laser microvias: Connect top-side BGA pads and traces to the adjacent layer.
  • L21–L22 laser microvias: Provide corresponding bottom-side connections.
  • Internal buried vias: Connect selected layers without reaching the finished outer surfaces.
  • L1–L22 plated through-holes: Provide full-depth connections where required.

When a signal microvia terminates on a ground-reference layer, its capture pad must be isolated from the surrounding ground copper and connected to the intended signal network.

1+20+1 versus 2+18+2 HDI construction

  • 1+20+1: Suitable when one buildup level on each side provides sufficient BGA breakout and internal routing access.
  • 2+18+2: Provides additional buildup connections for denser routing but requires more sequential lamination and microvia processing.

The appropriate construction depends on BGA escape routing, required layer transitions, and interconnect reliability. Additional buildup levels should address a specific routing limitation.

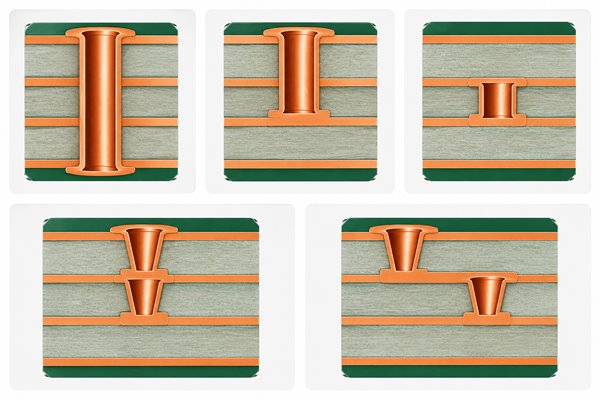
How Are Microvias, Buried Vias, and Via-in-Pad Designed for 22-Layer HDI PCBs?

22-layer HDI PCB via design must balance routing density, drilling depth, copper plating, and interconnect reliability.
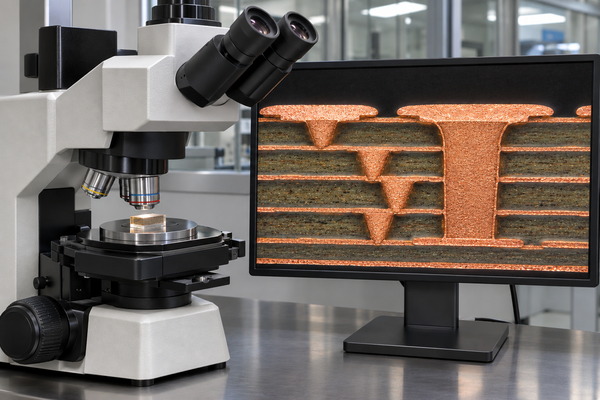
22-Layer HDI PCB, https://www.bestpcbs.com/blog/2026/11/22-layer-hdi-pcb/
  • Laser microvias: A 0.10 mm laser microvia provides a compact connection between adjacent buildup layers. Its feasibility depends on dielectric thickness, capture-pad dimensions, drilling geometry, and metallization. For example, a 0.10 mm laser-entry diameter with a 0.075 mm dielectric depth gives a nominal depth-to-diameter ratio of 0.75:1.

  • BGA via-in-pad: Filled and capped microvias allow routing beneath fine-pitch BGA pads. Copper filling, planarization, and capping must produce a flat, solderable surface. Voids or uneven capping can affect solder-joint quality.

  • Mechanical buried vias: An L2–L21 buried via may extend through most of the central structure. At approximately 2.0 mm drilling depth, a 0.20 mm drill diameter produces a 10:1 aspect ratio, while a 0.25 mm drill produces 8:1. If these dimensions represent finished holes, the actual drill sizes and aspect ratios must be recalculated.

  • Plated through-holes: Through-holes provide full-depth connections but consume routing space throughout the stackup. Unused portions of high-speed signal vias can create stubs, making antipad optimization or backdrilling relevant.

Deep buried-via manufacturability depends on hole-wall preparation and copper plating continuity. High aspect ratios make uniform copper deposition more difficult. The drilling and plating processes must therefore be evaluated against the actual hole depth, not simply the specified diameter.

What Are the Critical Design Requirements for a 22-Layer HDI PCB?

A 22-layer HDI PCB must meet its electrical, dimensional, and fabrication requirements within one approved construction.

The following represents a demanding high-speed PCB project.

Design Parameter Example Specification
PCB layers 22
Board dimensions 228.35 × 160 mm
Finished thickness 2.25 mm ±10%
HDI construction 1+20+1
Laser microvias 0.10 mm, L1–L2 / L21–L22
Mechanical buried vias 0.20 / 0.25 mm, L2–L21
Plated through-holes 0.25 mm
Minimum trace / spacing 85 / 100 µm
BGA pitch 0.8 / 1.0 mm
Inner signal copper 17 µm
Selected power-plane copper 35 µm
Outer copper 17 µm base, approximately 32 µm finished
Controlled impedance 40/50Ω single-ended; 80/100Ω differential, ±10%
High-speed interfaces SerDes up to 6.25 Gb/s; DDR3
Surface finish ENIG

These are example project requirements, not guaranteed manufacturing capabilities.

Three constraints require particular attention:

  • Fixed thickness: The approved 2.25 mm nominal thickness must accommodate all copper and dielectric layers. A ±10% finished-thickness tolerance does not authorize an unapproved change to the nominal stackup.
  • Fine-line geometry: An 85 µm trace must be evaluated against its finished copper thickness. Internal and external layers may require different etching compensation.
  • Impedance tolerance: A 40Ω ±10% requirement permits only ±4Ω deviation, which is tighter than a generic ±5Ω tolerance and requires specific capability confirmation.

Industrial boards may also contain hundreds of press-fit connector holes. For example, a VME board requiring 105 holes at 0.60 mm and 320 holes at 1.00 mm needs connector-specific finished-hole tolerances, plating specifications, and board-thickness compatibility.

ENIG used on BGA solder pads does not automatically qualify the finish inside every press-fit hole.

How Can Signal Integrity and Controlled Impedance Be Maintained in 22-Layer HDI PCBs?

Controlled impedance in a 22-layer HDI PCB depends on finished trace geometry, dielectric spacing, copper thickness, material properties, and reference-plane continuity.

For high-speed interfaces such as SerDes and DDR3, the main requirements are:

  • Finished conductor dimensions: Calculate impedance using etched trace geometry, copper thickness, and differential-pair spacing rather than nominal CAD dimensions alone.
  • Continuous reference planes: Keep critical signals over suitable references and provide appropriate return-current paths during layer transitions.
  • Controlled via transitions: Review capture pads, antipads, via barrels, and unused stubs that can introduce reflections.
  • Transmission-line loss: Evaluate material Df, copper roughness, channel length, and connector transitions against the required insertion-loss budget.
  • Manufacturing verification: Use representative impedance coupons to measure controlled-impedance structures under agreed test conditions.

For a 100Ω differential pair with ±10% tolerance, the acceptable measured range is 90–110Ω.

At 6.25 Gb/s NRZ signaling, the Nyquist frequency is approximately 3.125 GHz. Higher-frequency components also contribute to channel performance, making dielectric loss and via transitions important.

DDR3 interfaces additionally require suitable clock and data-strobe routing, timing margins, and termination.

Meeting impedance tolerance does not guarantee complete signal integrity. Coupon testing verifies selected fabricated transmission lines, while full-channel performance requires electrical simulation or system-level validation.

Which PCB Materials Are Suitable for High-Speed 22-Layer HDI Designs?

High-speed 22-layer HDI PCBs require laminates with suitable dielectric properties, thermal performance, available thicknesses, and compatibility with the specified HDI construction.

Common material options include:

Suitable for demanding high-speed digital applications. A published 0.051 mm core construction has Dk 3.30 and Df 0.0026 at 10 GHz. Other constructions have different values, so the selected core and prepreg specifications must be used for impedance calculations.

Used in high-speed networking, communication, and computing systems. Panasonic lists Dk 3.34 and Df 0.0037 at 13 GHz for its R-5775(N) construction. Other variants have different dielectric properties and available constructions.

  • Shengyi S7439 — Low-loss high-speed laminate

Suitable for servers, switches, networking equipment, and backplanes. Shengyi lists Dk 3.80 and Df 0.0068 at 10 GHz using the specified IPC test method. Material selection depends on the required channel-loss budget and stackup.

  • ITEQ IT-968G — Very-low-loss, high-Tg laminate

Used in high-speed networking and server applications. For a specified 55% resin-content construction, ITEQ lists Dk 3.59 and Df 0.0050 at 10 GHz. Other resin contents produce different dielectric values.

  • TUC TU-862HF — High-Tg, halogen-free laminate

Suitable for multilayer applications requiring thermal stability and halogen-free construction. Published data for a specified 50% resin-content construction includes Dk 4.4 and Df 0.010 at 1 GHz. These figures use different test conditions from the higher-frequency data above and should not be compared directly.

TU-862HF is not an automatic electrical replacement for I-Tera MT40 or MEGTRON 6.

Can materials be substituted without changing the original layout?

Substitution is possible only when the replacement satisfies the approved electrical and mechanical requirements.

  1. Recalculate the stackup: Select available core and prepreg constructions that maintain the specified board thickness.
  2. Recalculate impedance: Verify every controlled layer using the replacement material’s dielectric properties.
  3. Check signal loss: Confirm that the substitute satisfies the required high-speed channel-loss budget.
  4. Verify manufacturing compatibility: Evaluate lamination, thermal expansion, dimensional stability, and HDI processing.
  5. Confirm permitted compensation: Determine whether allowable conductor adjustments can meet impedance requirements without changing the approved routing.

For urgent prototypes, in-stock laminate materials may reduce sourcing delays. However, similar nominal Dk values do not guarantee equivalent impedance, insertion loss, or manufacturing behavior.

Material substitutions affecting the approved construction require customer confirmation.

What Are the Main Challenges and Solutions in 22-Layer HDI PCB Manufacturing?

22-layer HDI PCB manufacturing requires accurate layer registration, reliable interconnections, fine-line control, and dimensional stability.

The primary challenges and solutions are:

  • Multilayer registration errors

Challenge: Material movement during lamination can shift internal copper features and reduce alignment between buried vias and capture pads.

Solution: Apply material-specific dimensional compensation, controlled lamination conditions, and registration inspection before subsequent processing.

  • Deep buried-via plating defects

Challenge: High-aspect-ratio holes may develop nonuniform barrel copper or plating discontinuities.

Solution: Use drilling, desmear, and plating processes suitable for the actual hole depth. Verify barrel copper continuity through microsection inspection.

  • Microvia interface failures

Challenge: Poor target-pad preparation or insufficient metallization can create weak connections that may fail after thermal exposure.

Solution: Control laser drilling, pad preparation, copper deposition, filling, and capping. Apply structural and thermal reliability verification when required.

  • Fine-line and impedance variation

Challenge: Etching variation or uneven finished copper thickness can alter conductor geometry and impedance.

Solution: Apply copper-dependent etching compensation, measure finished trace dimensions, and verify impedance with representative coupons.

  • Board warpage and thickness variation

Challenge: Unbalanced copper distribution and dielectric construction can cause deformation during lamination.

Solution: Balance the stackup where practical, control lamination conditions, and inspect finished dimensions.

  • Press-fit connector-hole defects

Challenge: Incorrect hole dimensions or plating may damage connections during installation.

Solution: Follow the connector manufacturer’s finished-hole and plating requirements, supported by dimensional inspection.

How Are 22-Layer HDI PCBs Fabricated and Quality Tested?

22-layer HDI PCB fabrication involves inner-layer processing, buried-via construction, central lamination, outer HDI buildup, and final verification.
22-Layer HDI PCB, https://www.bestpcbs.com/blog/2026/11/22-layer-hdi-pcb/

For a typical 1+20+1 structure, the manufacturing stages are:

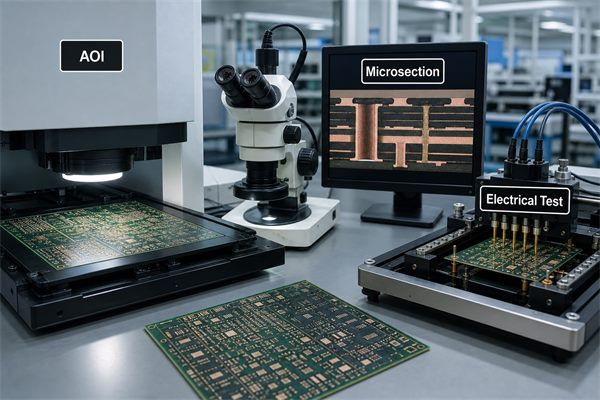
  1. Inner-layer fabrication: Image, etch, and inspect internal copper patterns using AOI.
  2. Buried-via processing: Drill, desmear, metallize, and plate internal connections before subsequent lamination makes them inaccessible.
  3. Central-structure lamination: Align and laminate the 20-layer central structure using the approved materials.
  4. HDI buildup: Add outer dielectric and copper layers, laser-drill microvias, and complete metallization, filling, and capping where specified.
  5. Final PCB processing: Complete applicable through-hole plating, outer-layer circuits, solder mask, ENIG, and profiling.

Quality verification includes:

  • Electrical testing: Detects opens and shorts in the completed circuitry.
  • Microsection inspection: Examines buried-via copper, microvia interfaces, layer registration, and filling quality.
  • Impedance testing: Measures specified transmission-line structures using representative coupons.
  • Dimensional inspection: Confirms finished thickness, board outline, and critical connector-hole dimensions.
  • Thermal reliability testing: Evaluates interconnect behavior under agreed thermal-stress conditions when required.

Inner-layer AOI is performed during fabrication to detect conductor defects before lamination.

The applicable IPC-6012 performance class and project-specific requirements determine the acceptance criteria. Inspection records and required reports should be agreed upon before manufacturing.

What Should You Consider When Prototyping a Complex 22-Layer HDI PCB?

22-layer HDI PCB prototyping should verify a construction that can be repeated during production, not merely demonstrate that a small number of boards can be fabricated.

Even a 3–4-piece prototype order may require extensive engineering preparation when the design contains deep buried vias, filled microvias, and strict mechanical requirements.

Before prototype release, confirm:

  • Stackup: Approved materials, dielectric thicknesses, copper weights, and layer assignments.
  • Via construction: Hole sizes, layer connections, and filling or capping requirements.
  • Impedance: Controlled layers, target values, tolerances, and permitted manufacturing compensation.
  • Mechanical specifications: Board dimensions, connector positions, finished-hole sizes, and critical tolerances.
  • Acceptance criteria: Required electrical, impedance, structural, and reliability verification.

Any necessary material substitution or manufacturing adjustment should be approved before fabrication. Maintaining the intended production construction during prototyping reduces the risk of further qualification or redesign.

What Is the Lead Time for 22-Layer HDI PCB Prototyping and Production?

The lead time for a 22-layer HDI PCB depends on material availability, manufacturing complexity, engineering approval, and testing requirements.

The main scheduling factors are:

  • Materials: Availability of specified laminate and prepreg constructions.
  • HDI buildup: Sequential lamination, laser drilling, microvia filling, and capping.
  • Buried vias: Specialized drilling and plating requirements for deep mechanical holes.
  • Engineering approval: Resolution of stackup, impedance, or mechanical conflicts.
  • Testing: Required impedance measurements, microsections, and reliability verification.

For urgent prototypes, complete fabrication data and approved material alternatives can reduce avoidable delays.

Prototype quantity alone does not determine lead time. A four-piece order may require the same critical processing stages as a larger production batch. Delivery should be confirmed after reviewing the approved construction, materials, and production capacity.

What Factors Affect 22-Layer HDI PCB Manufacturing Costs?

The cost of a 22-layer HDI PCB depends on materials, buildup structure, via complexity, fabrication tolerances, inspection, and order quantity.

The main cost drivers include:

  • HDI buildup: Additional lamination and laser-drilling operations.
  • Via construction: Deep buried holes and filled or capped microvias.
  • Materials: Low-loss laminates and specialized dielectric constructions.
  • Fine-line fabrication: Tight conductor dimensions and reduced manufacturing margins.
  • Quality verification: Additional impedance testing, microsections, and reliability checks.
  • Order quantity: Engineering and setup costs spread across fewer prototype boards.

Cost optimization options include:

  • Use 1+20+1 instead of a higher-order buildup when routing permits.
  • Avoid filled vias where they are not needed for electrical or assembly requirements.
  • Review noncritical tolerances that unnecessarily restrict manufacturing.
  • Consider approved materials already available for production.
  • Maintain a consistent construction between prototypes and later batches.

Any adjustment must preserve the required electrical performance, mechanical fit, and interconnect reliability.

Why Choose EBest Circuit for 22-Layer HDI PCB Manufacturing?

For a complex 22-layer HDI PCB, you need clear answers about manufacturing feasibility, material availability, quality verification, and delivery before placing an order.

EBest Circuit provides multilayer PCB fabrication, HDI manufacturing support, DFM review, and PCB assembly services.

We can help you:

  • Identify manufacturing conflicts before production: Submit your fabrication files for a free DFM check covering via depth, copper thickness, dielectric construction, and mechanical tolerances.

  • Evaluate complex HDI requirements: Our capability information includes special multilayer constructions up to 32 layers and laser blind vias down to 0.10 mm. We assess the complete proposed structure rather than relying only on individual process limits.

  • Review material alternatives: If the specified laminate is unavailable, we can evaluate candidate materials against the approved impedance, thickness, and manufacturing requirements.

  • Clarify quality verification: Define the required electrical tests, impedance measurements, microsections, and dimensional inspection records before production.

  • Support prototype-to-production continuity: Maintain the approved manufacturing revision, material specifications, and critical construction requirements for subsequent orders.

  • Combine PCB fabrication and assembly: We also provide SMT assembly, component sourcing, and specified testing for customers requiring complete PCBAs.

For demanding 22-layer 1+20+1 HDI PCB projects, our engineering team can review the fabrication package and confirm the feasible manufacturing approach, quotation, and lead time.

FAQs About 22-Layer HDI PCB Design & Manufacturing

Q1: Can an NDA be signed before sharing confidential PCB files?

A1: Yes. Customers can request a non-disclosure agreement before submitting confidential design information. The terms and file-handling conditions should be agreed upon before technical data is exchanged.

Q2: Is IPC Class 3 required for every 22-layer HDI PCB?

A2: No. The acceptance class depends on the product’s intended use and contractual reliability requirements. A 22-layer construction does not automatically require Class 3.

Q3: Can individual prototypes be serialized for traceability?

A3: Serial-number marking can be specified in the fabrication requirements. The marking location, format, and required traceability records should be confirmed before manufacturing.

Q4: What happens if Gerber files and drill drawings contain different revisions?

A4: Fabrication should not begin until the discrepancy is resolved. One approved revision must control the artwork, drilling data, stackup, and fabrication notes.

Q5: Can customer-supplied laminate materials be used?

A5: Customer-supplied materials may be evaluated for identification, condition, traceability, dimensions, and process compatibility. Acceptance must be confirmed before fabrication.

Q6: Can different PCB designs be combined into one manufacturing panel?

A6: Mixed-design panelization may be possible when the boards have compatible materials, thicknesses, copper constructions, and processing requirements. Different HDI structures may prevent combined production.

Q7: Can special packaging be requested for finished HDI PCBs?

A7: Yes. Customers can specify individual board protection, moisture-control packaging, labeling, and other handling requirements appropriate to the product and shipping conditions.

Q8: Can a certificate of conformity be supplied with the PCB order?

A8: A certificate of conformity can be requested as part of the agreed delivery documentation. It should identify the relevant order, product revision, and applicable acceptance requirements.

Q9: Which surface finish should be specified for a 22-layer HDI PCB?

A9: The finish should be selected for the component termination, assembly process, storage period, flatness needs, and reliability requirements. Confirm the permitted finish and thickness in the fabrication notes before quotation.

Q10: Can a 22-layer HDI PCB include edge plating or castellated features?

A10: These features may be feasible, but their geometry, copper coverage, board-edge clearance, panelization, and inspection requirements must be reviewed with the complete stackup and outline data.


Are you developing a 22-layer HDI PCB with dense BGA routing, deep buried vias, controlled impedance, or fixed mechanical dimensions? EBest Circuit can review your design requirements and assess manufacturing options for prototypes and production.

Send your Gerber or ODB++ files, stackup, drill specifications, material requirements, quantity, required delivery date, and delivery location to sales@bestpcbs.com. Request a free DFM check and a quotation for your custom 22-layer HDI PCB project.
You may also like

What Is Sequential Lamination in PCB and How Does It Work?
Thursday, September 17th, 2026

Sequential lamination builds a PCB in two or more controlled lamination stages so internal vias can be formed before later layers make them inaccessible. The practical question is not how many layers the board has. It is which blind, buried, or microvia connections must be completed at each stage and what those choices mean for reliability, cost, and lead time.

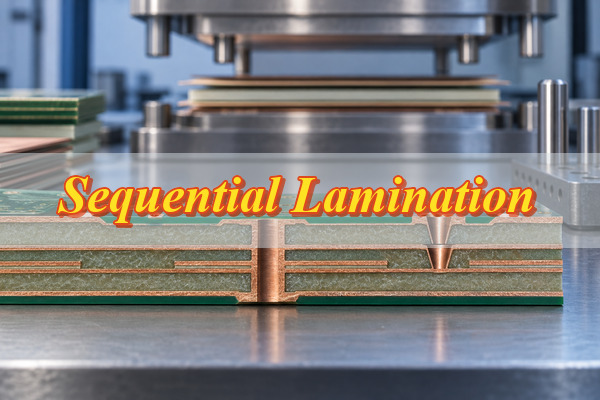
sequential lamination, multilayer PCB cross-section beneath a lamination press

What Is Sequential Lamination in PCB?

A conventional multilayer PCB is usually bonded as one prepared stack. Sequential lamination pauses the build, forms connections in an accessible partial structure, adds another layer set, and continues outward.

A buried via can therefore be drilled and plated before later layers enclose it. Multi-level microvias follow the same logic: each lower tier is completed before the next dielectric covers its landing layer.

The deciding test is layer access. Trace every via from its drilling side to its target layer. If that connection can still be formed after the main bond, another build stage may be unnecessary. If the target becomes enclosed first, the stack must be divided into accessible substructures. Sequential lamination is therefore a construction sequence, not a performance grade.

How Is Sequential Lamination Different From Standard PCB Lamination?

The difference is when the internal connections are made. Standard construction completes most internal preparation before one main multilayer bonding stage. Sequential construction inserts drilling, plating, filling, or inspection between bonding stages.

Factor Standard Multilayer Lamination Sequential Lamination
Lamination process Mainly one multilayer bonding stage Two or more controlled build stages
Via structures Mainly through vias and structures accessible after bonding Buried vias, blind vias, and multi-level microvias
Layer access Internal layers become inaccessible after bonding Selected layers remain accessible between stages
Process complexity Lower when it meets the design Higher because controlled operations repeat
Cost and lead time Generally lower Generally higher
Typical use Conventional multilayer PCB HDI and complex internal via structures

A high layer count does not by itself require sequential lamination. A board with many layers and only plated through holes may use a conventional build, while a board with fewer layers but a buried via or several microvia tiers may need staged construction.

When Does a PCB Design Require Sequential Lamination?

Sequential lamination becomes necessary when a required connection cannot be drilled, plated, filled, or verified after the full stack has been bonded. Four design situations commonly create that condition:

  • Buried vias that would be sealed inside the finished stack: the via must be completed in a core or sub-composite while both target layers are still exposed.
  • Multiple HDI build-up layers: each added dielectric can create a new microvia level that must be formed before another layer is added.
  • Stacked or multi-level microvias: the lower microvia usually needs controlled plating, filling, and a planar landing surface before the upper level is built.
  • Fine-pitch BGA escape that cannot reasonably use through vias: adjacent-layer microvias can release routing area, but their start and stop layers determine the build sequence.

High layer count and the HDI label are not sufficient reasons by themselves. Hide the outer layers in the stackup view, add them back in build order, and note where a connection loses access before it is complete. That via map reveals whether staged construction is necessary and whether a routing change could remove a build-up tier.

How Does the Sequential Lamination Process Work?

The process follows the changing access to each via target. It starts with the innermost structure, adds a layer set, completes the connections that are accessible at that point, and repeats only when the stackup requires another tier.

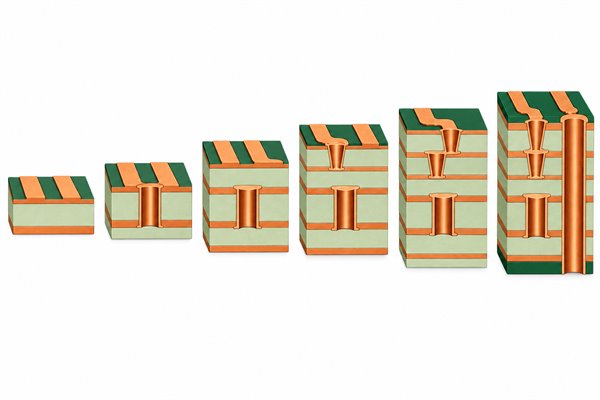
sequential lamination, six-stage PCB build sequence on a white background
  1. Document the stackup and via spans. Identify every copper layer, dielectric, via start and stop layer, fill requirement, and controlled-impedance reference. The output is a build diagram that can be checked before routing is frozen.
  2. Build the initial core or sub-composite. Image and etch the inner copper, then align the partial structure. The layers that will support internal vias remain reachable.
  3. Drill and plate the internal vias. Form the buried holes or first accessible connections, then clean, metallize, fill, and inspect them as required. Their conductive path is complete before enclosure.
  4. Laminate the next layer pair or build-up layer. Add dielectric and copper to the verified partial structure. The result is a larger stack with a new outer surface available for processing.
  5. Form the next blind or microvia level. Drill and plate the newly accessible tier, using filling or planarization where another via must land above it. This completes the next connection level.
  6. Repeat as required and finish the PCB. Continue the add-layer-and-connect sequence for the remaining tiers, then complete final through holes, outer-layer processing, solder mask, finish, profiling, and the agreed testing.

This sequence explains the design consequence: adding or extending one via span can change the required build stages. It may add a fill dependency, alter which layer must remain exposed, or require another controlled cycle.

For the designer, the useful output is a confirmed build diagram: layer order, via levels completed at each stage, landing surfaces required by the next tier, and any geometry or material limit that changes the stackup.

How Do Different Via Structures Affect the Lamination Sequence?

Each via must be formed while its drilling side and target layer are accessible. The name of the via helps describe the connection, but the exact start-stop layers and stacking arrangement determine the sequence.

sequential lamination, cross-sections of through blind buried stacked and staggered vias
  • Through vias: these normally pass through the completed stack and can be drilled after final lamination, so they do not create a sequential stage by themselves.
  • Buried vias: these connect internal layers and must be processed before later layers hide both ends.
  • Blind vias: these connect an outer surface to an internal target. Their route depends on the depth, dielectric thickness, drill method, and stage at which the target is exposed.
  • Single-level microvias: these usually connect adjacent layers through a thin dielectric and may fit within one build-up stage.
  • Stacked microvias: the upper microvia lands directly above the lower one, creating a fill and planarity dependency between tiers.
  • Staggered microvias: the levels are offset, which avoids a direct via-on-via interface but does not necessarily remove the need to build each dielectric tier in sequence.

Do not assign a cycle count from terms such as blind via or HDI alone. Two boards can use the same via label yet require different sequences because the vias stop on different layers or use different fill and stacking arrangements.

How Does the PCB Stackup Determine the Number of Lamination Cycles?

The cycle count follows the number of connection groups that must be completed before another layer blocks access. Total layer count matters less than the order in which via targets disappear inside the stack.

Notation such as 1+N+1 or 2+N+2 shows the build-up layers around a core region, but it does not prove a universal press count. The core may contain buried vias, and outer tiers may be stacked, staggered, symmetric, or one-sided. The notation shows the layer arrangement; the via start-stop map shows the build dependencies.

Three simplified cases show how that logic changes the build:

  • Eight-layer board with through vias only: the prepared layers can normally be bonded in the main multilayer lamination, followed by through-hole drilling. The layer count does not create another stage by itself.
  • Core containing buried vias: the internal via is drilled and plated while its core or sub-composite is accessible. Outer layers are laminated only after that connection is complete, so the via architecture creates a staged build.
  • 2+N+2 HDI with stacked microvias: the first microvia tier must be formed before the second build-up dielectric covers it. Direct stacking can also require a filled, planar lower via before the upper tier is added.

Estimate the sequence from the inside out:

  1. Map every start and stop layer. Separate through, blind, buried, and microvia spans.
  2. Group connections that are accessible together. Vias that can be formed in the same exposed sub-composite may share a stage.
  3. Mark each covering event. When a new dielectric hides a completed target, record the lamination needed before that happens.
  4. Add stacking dependencies. A microvia tier that needs a filled, planar lower via must be completed before the next tier can begin.

If two proposed builds show different cycle counts, compare their layer-by-layer diagrams, via formation stages, and fill sequence before treating either number as correct.
What Should You Check Before Finalizing a Sequential Lamination Stackup?

Review the stackup before dense routing makes the construction difficult to change. The goal is to prove that every added tier solves a real routing or electrical constraint and that its build dependency is understood.

  • Via start and stop layers: make the CAD data, drill table, and cross-sectional stackup agree.
  • Stacked or staggered arrangement: confirm whether direct stacking is necessary or an offset path can meet routing and reliability needs.
  • Number of build-up tiers: test whether a routing change, another conventional layer, or a different escape pattern can remove a tier.
  • Material system: check whether cores, prepregs, build-up dielectrics, and copper constructions suit the planned press and assembly thermal history.
  • Impedance and reference layers: protect return paths, reference-plane continuity, dielectric targets, and any backdrill requirement when the build changes.
  • Reliability requirements: state the product environment, assembly exposure, acceptance class, coupon needs, and qualification expectations.

Generic online limits should not be copied directly into CAD rules. Usable geometry depends on the material, dielectric thickness, copper, drill and fill process, registration capability, and product requirement. For a useful DFM or quotation review, send the stackup, via map, fabrication data, quantity, and reliability requirements together.

How Can Multiple Lamination Cycles Affect PCB Reliability?

Extra cycles add thermal, pressure, and registration exposure. That does not make a sequentially laminated PCB unreliable by definition, but it reduces the value of judging the design by layer count or a room-temperature electrical test alone.

Risk area Why multiple cycles matter What to verify
Microvia interface Repeated thermal exposure can reveal weak plating, fill, or target-pad interfaces Via structure, fill route, representative coupons, and qualification method
Layer registration Alignment error can accumulate as more structures are bonded Capture pads, registration allowance, and evidence from intermediate stages
Material thermal history The laminate experiences repeated heat and pressure before assembly reflow Material suitability for the full fabrication and assembly history

Risk is often concentrated at interfaces: a microvia base meeting its target pad, a filled via supporting an upper tier, or resin bonding around uneven copper. Residue, voids, weak plating, poor planarity, expansion mismatch, and registration error can reduce margin during reflow or thermal cycling.

Qualification should represent the connections with the greatest structural dependency. Match the coupon or test vehicle to the microvia tiers, target-pad interfaces, fill arrangement, materials, and expected assembly exposure. A room-temperature continuity check confirms a path at that moment; it does not reproduce repeated reflow or service thermal cycling.

How Does Sequential Lamination Affect PCB Cost and Lead Time?

Cost and lead time usually rise because pressing, drilling, plating, filling, planarization, and inspection may repeat for each build stage. There is no reliable universal percentage; the impact depends on the stackup, material, panel use, via density, registration demand, testing, and quantity.

  • Repeated controlled operations: each added tier consumes equipment time and requires another alignment and processing sequence.
  • Fill and planarization: stacked structures may need a prepared landing surface before the next level can be formed.
  • Intermediate verification: hidden circuitry and via quality need to be checked before the next layer removes access.
  • Longer dependency chain: later work cannot begin until the preceding structure is complete and suitable for the next tier.
  • Greater late-stage loss: a defect found after several completed stages affects more accumulated processing than an early defect.
The best cost reduction is often one unnecessary build-up tier removed before layout release. Compare alternatives that preserve the same electrical and mechanical requirements, such as fewer unique via spans, staggered rather than stacked microvias, a different BGA escape, or an added conventional layer.

FAQs About Sequential Lamination Technology

Q1: What files help a supplier quote the actual build instead of making assumptions?

A1: Send one consistent data package. Include Gerber or ODB++ data, NC drill data, a controlled stackup, via start-stop layers, finished copper weights and board thickness, material and impedance requirements, via-fill or cap requirements, acceptance and test expectations, quantity, and target delivery date.

Q2: How should blind and buried via spans appear in the drill data?

A2: Every start-stop layer pair must be unambiguous. Separate drill files or a clearly mapped drill table can be used, but each span should identify its layer pair, plated status, finished size, tolerance, and any fill or cap requirement. The naming convention matters less than agreement between the drill data, stackup, and fabrication drawing.
Q3: Can stacked microvias be changed to staggered microvias without design approval?

A3: No. The alternative may improve the build margin, but it changes pad locations, routing space, and possibly reference-plane or impedance conditions. It should be proposed as a documented DFM change and approved in the controlled design data before production.

Q4: Why can two PCB quotations use different build sequences?

A4: The suppliers may be working from different assumptions or grouping operations differently. Compare the annotated build diagrams, via spans, fill and planarization route, materials, impedance construction, and test scope. A lower cycle number is not automatically the better or equivalent proposal.

Q5: Can an enclosed buried-via defect be repaired after final lamination?

A5: It is generally not a practical local rework. The connection is trapped inside the bonded stack, so opening it can damage surrounding layers and dielectric. Intermediate inspection, representative coupons, and final electrical testing are used to find problems; an affected bare board is usually rejected or rebuilt rather than patched.

Ready to build a sequential-lamination PCB? Send your stackup, Gerber or ODB++ files, via map, material and impedance requirements, quantity, and target delivery date to sales@bestpcbs.com. EBest Circuit can review the proposed construction and prepare a PCB quotation based on the actual build sequence.

You may also like

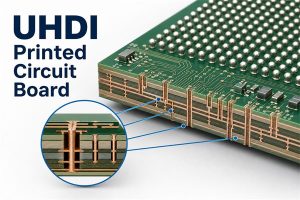
UHDI Printed Circuit Board: Design Rules, Stackup, and DFM
Tuesday, September 1st, 2026

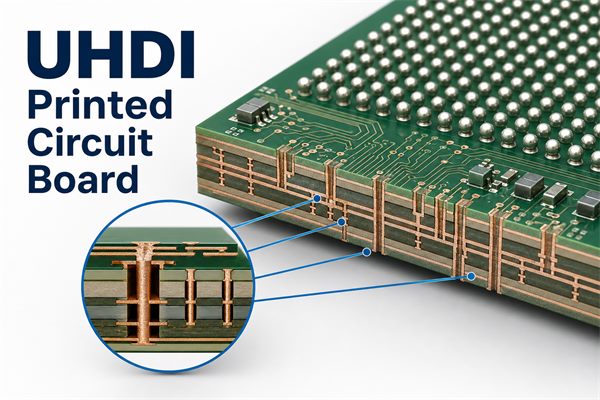
A UHDI printed circuit board moves beyond conventional HDI when at least one critical feature enters the ultra-fine range. That change affects far more than trace width. The imaging method, copper build, microvia geometry, dielectric thickness, registration plan, solder mask, inspection criteria, and assembly interface must be treated as one manufacturing system.

This guide helps design and procurement teams decide whether a project is truly UHDI, where early DFM work prevents redesign, and what evidence should be agreed before prototype release. It also separates published working thresholds from a supplier’s confirmed production capability—an important distinction when yield, reliability, and repeatability matter.

UHDI printed circuit board with ultra-fine traces and laser microvias

What Is a UHDI Printed Circuit Board?

UHDI means ultra-high-density interconnect. The industry’s working definition generally places a board in UHDI territory when one or more features go beyond the highest conventional HDI producibility range. Common reference thresholds include:

  • Conductor line width below 50 µm.
  • Conductor spacing below 50 µm.
  • Build-up dielectric thickness below 50 µm.
  • Laser microvia diameter below 75 µm.

These figures are useful screening points, not permission to combine every minimum on one design. A board with 45 µm spacing on one layer may require a different process route from a board with 60 µm traces and 50 µm microvias. Material, copper thickness, panel format, feature distribution, registration tolerance, surface finish, and annual volume all affect the real production window.

The shorter phrase ultra hdi pcb often refers to the same technology. In practice, the fabrication drawing should state the actual features and acceptance requirements instead of relying on the label alone.

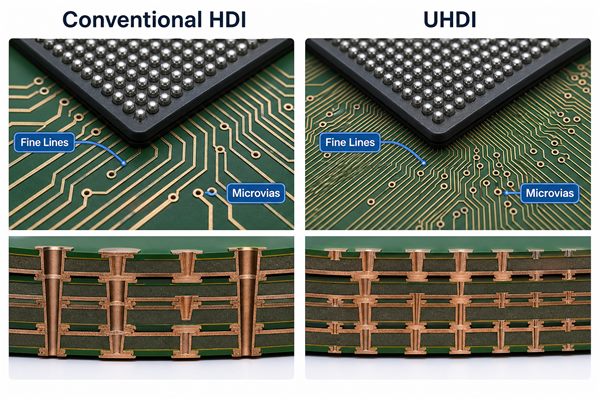
How Does UHDI Differ from Conventional HDI?

Conventional HDI gains density through laser microvias, blind or buried connections, sequential lamination, and via-in-pad. UHDI keeps those concepts but pushes selected geometries beyond conventional HDI process limits. That shift changes both the fabrication method and the amount of process verification required.

Design Area Conventional HDI UHDI Consideration
Fine conductors Often produced by optimized subtractive etching May require mSAP, SAP, or another ultra-fine-line process
Microvias Laser-drilled vias commonly around the 0.10 mm class Smaller geometry needs tighter drilling, plating, and registration control
Dielectrics Build-up films selected around a proven HDI stackup Very thin dielectrics make copper balance and via aspect ratio more sensitive
Inspection AOI, electrical test, impedance test, and microsection as specified More detailed coupons, dimensional evidence, and agreed acceptance rules may be needed

A designer should therefore ask, “Which features require UHDI?” rather than applying ultra-fine geometry across every layer. Restricting the most demanding rules to the package escape or other density-critical zones can improve yield and cost without sacrificing electrical performance.

HDI PCB Design Guidelines for UHDI Layouts

Useful hdi pcb design guidelines begin with the fabricator’s production window, not the CAD tool’s minimum setting. The following decisions should be closed before routing is frozen:

  • Define the density driver. Record BGA pitch, pad diameter, escape count, available routing channels, and the layers that genuinely need ultra-fine features.
  • Use regional rules. Keep wider traces and spaces outside dense package fields where possible. A mixed-rule design is usually easier to control than a board built entirely at the minimum.
  • Separate line and space values. Do not assume a supplier’s minimum line width automatically permits the same minimum clearance after plating.
  • Coordinate copper with geometry. Thicker copper is harder to resolve into very fine conductors. Base copper and final copper must both appear in the fabrication notes.
  • Treat solder mask as a precision layer. Mask registration, dam width, pad definition, and via treatment can determine whether fine-pitch assembly is practical.
  • Control impedance from the real stackup. Trace geometry, dielectric thickness, resin content, copper profile, and reference-plane distance must be reviewed together.

Do not design every feature at a supplier’s stated limit. The published minimum may describe a test coupon or a restricted build, while the stable production value may be wider. A useful DFM conversation distinguishes prototype feasibility, repeatable production, and the conditions attached to each.

Comparison of conventional HDI and UHDI PCB trace and microvia geometry

HDI PCB Stackup Decisions for UHDI

An hdi pcb stackup cannot be finalized independently from the escape strategy. The number of build-up layers, microvia spans, plane assignment, material family, and impedance targets determine the lamination sequence and the inspection plan.

Review these points together:

  • Build-up architecture: confirm whether 1+N+1, 2+N+2, any-layer, or another construction is actually required.
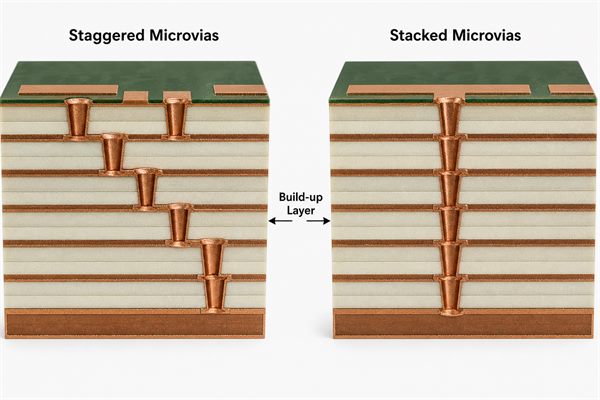
  • Microvia type: use staggered microvias where routing permits; specify stacked structures only where density justifies the additional process and reliability burden.
  • Via aspect ratio: match microvia diameter to dielectric depth. A small opening through an unnecessarily deep dielectric creates plating risk.
  • Via fill and cap: via-in-pad normally requires a defined fill, planarization, and cap-plating sequence before component assembly.
  • Stack symmetry: balance copper and dielectric construction to reduce bow, twist, and registration drift through repeated thermal cycles.
  • Material availability: confirm the exact laminate, build-up film, copper foil profile, thickness tolerance, and approved substitutes before impedance values are released.

Early stackup review is especially important when UHDI routing is combined with high-speed interfaces. Our existing guide to HDI PCB structures explains conventional 1+N+1, 2+N+2, and every-layer interconnect concepts, while the separate 80 GHz UHDI PCB article focuses on RF material and impedance concerns.

UHDI PCB stackup showing staggered and stacked laser microvias

How Does the HDI PCB Manufacturing Process Change for UHDI?

The hdi pcb manufacturing process normally uses sequential build-up, laser drilling, copper deposition, imaging, plating, lamination, and electrical verification. UHDI adds tighter interactions between these steps and may change the conductor-forming method.

  1. Engineering review: identify every sub-50 µm feature, microvia span, impedance structure, copper requirement, and inspection coupon.
  2. Material and process selection: choose a laminate, build-up dielectric, copper foil, and imaging route that can hold the requested geometry.
  3. Core and build-up imaging: form fine conductors with a process selected for the target line, space, and copper thickness.
  4. Laser drilling and desmear: control via diameter, taper, landing accuracy, and the condition of the target pad.
  5. Metallization and filling: establish reliable copper in the microvia, fill specified structures, and planarize via-in-pad surfaces.
  6. Sequential lamination: repeat build-up cycles while controlling registration, resin flow, copper balance, and thickness.
  7. Surface formation: apply solder mask and surface finish without consuming the clearances needed for fine-pitch assembly.
  8. Inspection and test: use AOI, electrical testing, microsection, dimensional measurement, impedance testing, or other project-specific evidence.

Subtractive etching can support some near-UHDI geometries, but very fine and consistent conductors may require modified semi-additive or semi-additive processing. The correct route depends on feature size, copper thickness, layer location, panel scale, volume, and supplier capability. It should be confirmed before the layout is locked.

Which DFM Risks Cause UHDI Prototype Failure?

UHDI prototypes most often become expensive when a local density decision triggers an unplanned process change. The risk is rarely one number in isolation.

  • Minimum geometry used everywhere: reduces the process margin across the whole panel even though only a small BGA area needs it.
  • Excessive stacked microvias: increases lamination count and concentrates thermo-mechanical stress.
  • Unconfirmed copper build: fine lines may not survive the plating and etching sequence at the requested final copper.
  • Ambiguous via notes: missing fill, cap, target-layer, or aspect-ratio requirements can change both cost and reliability.
  • Late impedance modeling: forces trace-width or dielectric changes after routing is complete.
  • Insufficient mask clearance: causes assembly constraints even when the copper pattern can be fabricated.
  • No agreed acceptance plan: leaves the customer and supplier evaluating fine features with different criteria.

A strong DFM response should show what must change, why it matters, and whether the recommendation affects electrical performance. “Cannot build” is not enough; the customer needs an alternative feature, stackup, or process route.

What Inspection Evidence Should Be Defined?

Electrical continuity alone cannot prove that a UHDI process is stable. The inspection plan should follow the critical risks in the design and may include:

  • AOI coverage for fine-line layers.
  • Microsection locations that represent stacked or staggered microvias.
  • Measurement of finished line width, spacing, dielectric thickness, and via geometry.
  • Impedance coupons that match the controlled layers and copper construction.
  • Electrical test coverage and netlist source.
  • Surface-finish thickness or wire-bond acceptance criteria when applicable.
  • Assembly X-ray or other inspection for fine-pitch packages when the project includes PCBA.

At EBest Circuit, our documented quality resources include AOI, electrical testing, impedance testing, microsection inspection, copper-thickness testing, 2D measurement, and X-ray inspection for relevant assembly work. The final test plan still depends on the product, customer specification, and confirmed process route. See our PCB quality and testing overview for the broader control framework.

UHDI PCB microsection and automated optical inspection workflow

How Do UHDI Choices Affect Cost and Lead Time?

UHDI does not automatically make the lowest system cost, even when it reduces board area. Cost and lead time rise when a design adds specialized material, semi-additive conductor formation, more lamination cycles, stacked microvias, tight registration, extra coupons, or low-yield feature combinations.

The practical cost levers are:

  • How many layers actually need ultra-fine line and space.
  • Whether a standard panel and material construction can be used.
  • The number of sequential lamination cycles.
  • Staggered versus stacked microvia architecture.
  • Base and finished copper thickness.
  • Surface finish and fine-pitch assembly requirements.
  • Prototype quantity, test evidence, and volume forecast.

A compact UHDI board can still lower total product cost when it removes connectors, reduces board area or layer count, shortens critical interconnects, or enables a smaller enclosure. The comparison should therefore use total system impact, not PCB unit price alone.

What Should Be Included in a UHDI RFQ Package?

Provide enough information for the supplier to evaluate the exact feature combination. A useful package includes:

  • Gerber or ODB++ fabrication data and the fabrication drawing.
  • Proposed layer stackup, material family, finished thickness, and copper weights.
  • A list of the minimum line, minimum spacing, smallest microvia, and affected layers.
  • Microvia spans, stacked or staggered structure, via fill, and cap-plating notes.
  • Controlled-impedance table and reference-layer information.
  • Surface finish, solder mask, legend, and assembly constraints.
  • Test standard, inspection evidence, coupon requirements, and acceptance class.
  • Prototype quantity, expected annual volume, and requested delivery date.
  • BOM, pick-and-place data, and assembly drawing when PCBA is required.

For a general supplier overview, you can also review our existing UHDI PCB fabrication page. Its purpose is supplier selection, while this page is intended to help engineering teams prepare a manufacturable design package.

FAQ About UHDI Printed Circuit Boards

Is every board with microvias a UHDI PCB?

No. Microvias are common in conventional HDI. UHDI is associated with one or more features beyond conventional HDI thresholds, such as sub-50 µm lines or spaces, sub-50 µm build-up dielectrics, or microvias below the 75 µm range.

Does UHDI always require mSAP?

No. The conductor-forming method depends on the target geometry, copper thickness, layer, panel, and supplier. Some near-UHDI features may be possible with advanced subtractive control, while tighter and more uniform conductors may need mSAP or SAP.

Are stacked microvias better than staggered microvias?

Not automatically. Stacked microvias save routing area, but they add process complexity and reliability sensitivity. Use them where density requires them; use staggered structures where the layout allows a more forgiving construction.

Can standard HDI design rules be reused for UHDI?

They are a starting point, not a release condition. UHDI requires a supplier-specific review of fine-line formation, dielectric depth, via geometry, copper build, registration, solder mask, inspection, and production volume.

How Can EBest Circuit Review Your UHDI Project?

EBest Circuit has provided PCB and PCBA support since 2006. We work with customers on PCB design review, prototyping, multilayer and HDI fabrication, component sourcing, assembly, and testing. Our documented management and compliance resources include ISO 9001:2015, ISO 13485:2016, IATF 16949, AS9100D, UL, RoHS, and REACH; applicability should be confirmed for the specific product and production route.

For a true UHDI request, we do not treat a marketing label as a capability approval. Our team first reviews the line and space by layer, dielectric construction, microvia geometry, copper build, stackup, impedance, surface finish, quantity, and required evidence. We then confirm whether the project fits an available process route or needs design adjustment. You can also review our broader PCB manufacturing capability information.

Send your Gerber or ODB++ files, stackup, impedance table, fabrication drawing, quantity, and test requirements to sales@bestpcbs.com. We will help identify the density-critical features, return practical DFM feedback, and confirm a manufacturable path for your UHDI printed circuit board before quotation.

You may also like

14-Layer HDI PCB: Stackup, Design Rules & Manufacturing Guide
Wednesday, August 19th, 2026

A 14 layer HDI PCB combines 14 copper layers with high-density interconnect features such as microvias, blind and buried vias, sequential lamination, and via-in-pad.

The extra layers provide room for signals, ground planes, and power distribution. HDI technology solves the routing problem around fine-pitch components, where conventional through vias consume too much board space.

Before selecting this structure, engineers usually need to determine:

  • How many HDI buildup layers are necessary?
  • Can the BGA be routed without stacked microvias?
  • Which stackup supports the required impedance?
  • Can the laminate tolerate repeated lamination?
  • Which fabrication limits should be confirmed before layout is frozen?

These choices have a larger impact on cost and manufacturability than the layer count alone.

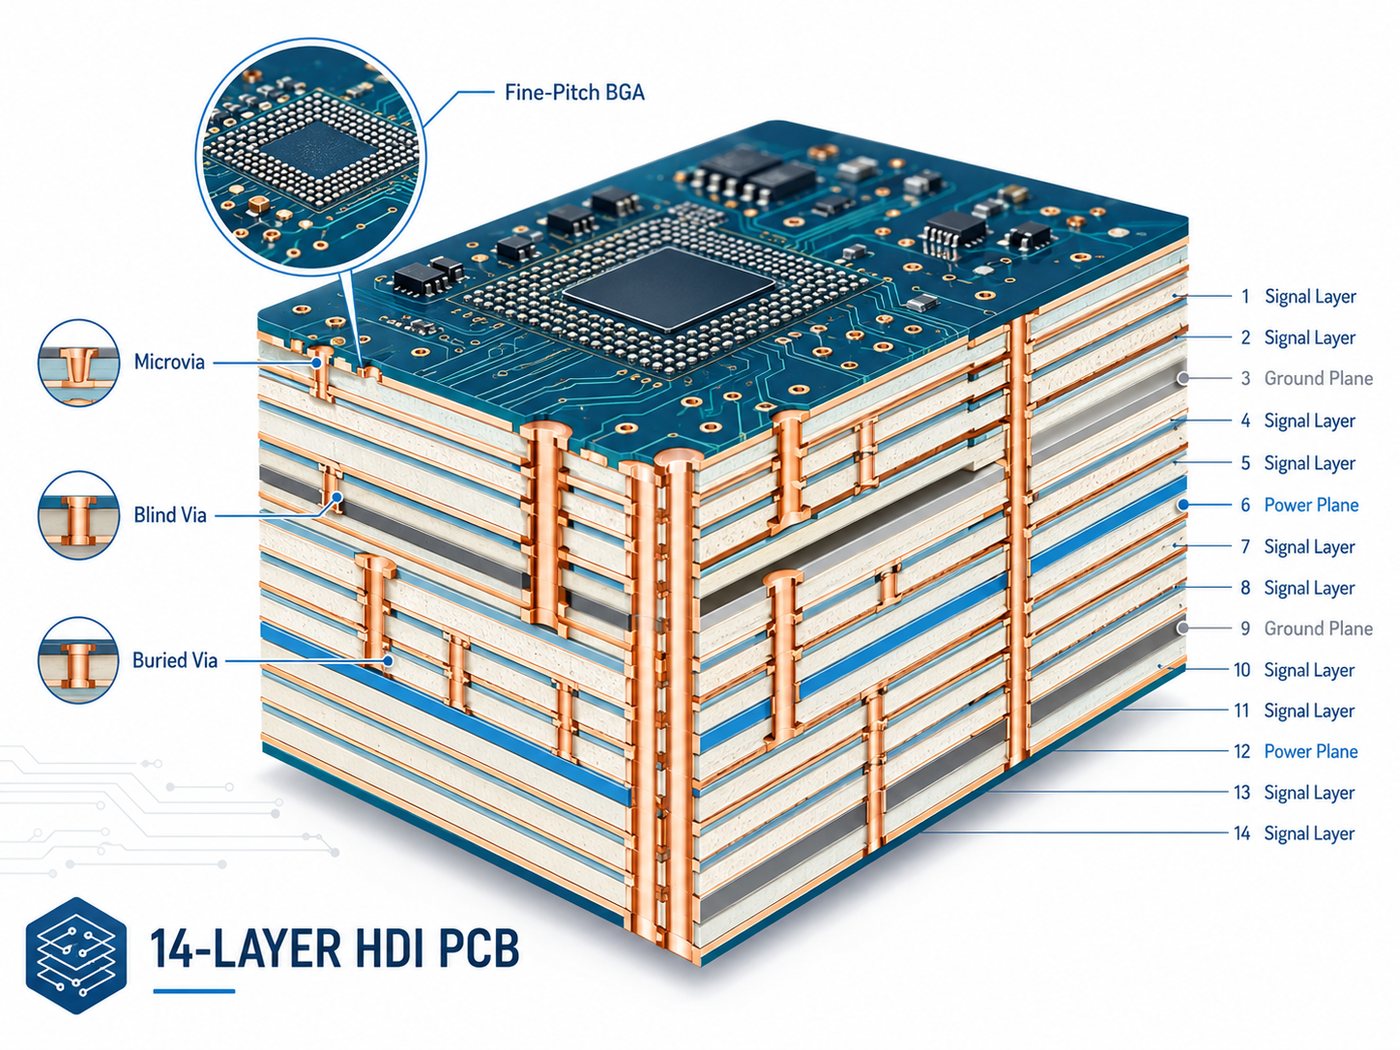
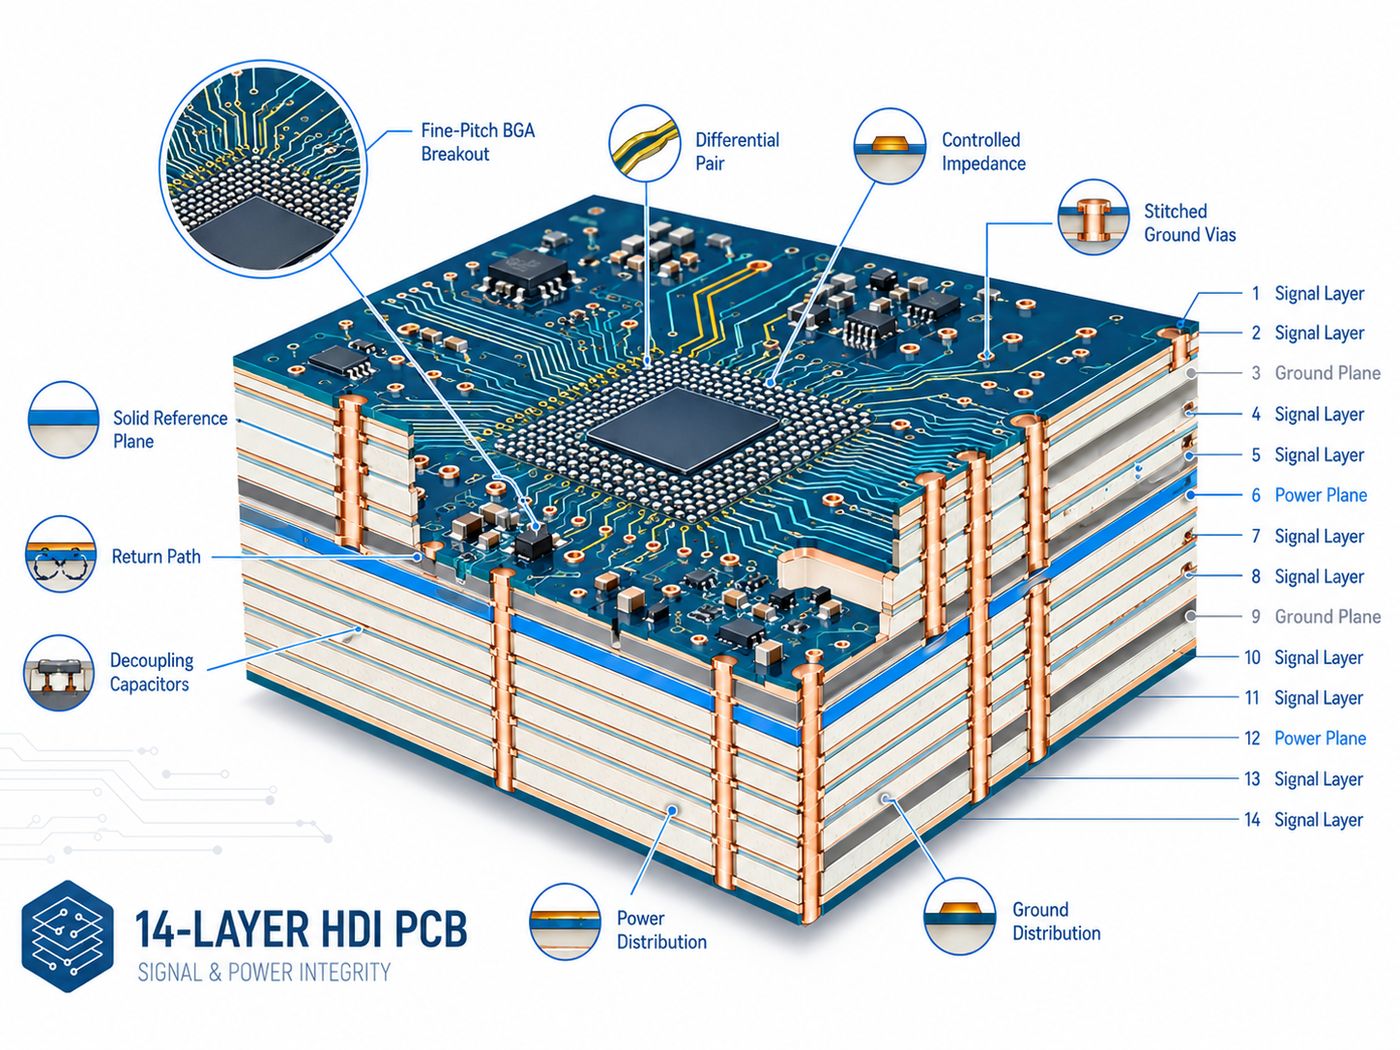
14-layer HDI PCB cutaway showing microvias, blind vias, buried vias, signal layers, ground planes and power planes

What Is a 14-Layer HDI PCB?

A 14-layer HDI PCB has 14 conductive copper layers and uses high-density vias to connect selected layers.

Common HDI features include:

  • Laser-drilled microvias
  • Blind and buried vias
  • Via-in-pad
  • Stacked or staggered microvias
  • Sequential buildup layers

A conventional 14 layer PCB can also have 14 copper layers but rely mainly on through vias.

HDI becomes useful when a design needs more routing channels around fine-pitch BGAs, processors, FPGAs, or other dense packages. If component pitch is generous and board area is not constrained, a conventional multilayer board may be the more economical choice.

When Do You Need a 14-Layer HDI PCB?

A 14-layer HDI construction makes sense when routing density, board size, and electrical requirements begin competing for the same space.

Typical cases include:

  • Fine-pitch BGA breakout
  • High-I/O processors or FPGAs
  • Compact communication or computing boards
  • Multiple high-speed interfaces
  • Designs requiring several continuous reference planes
  • Dense layouts where through vias block inner-layer routing

HDI should solve a specific layout problem. If a standard 14-layer board can meet routing and electrical requirements without microvias or sequential buildup, adding HDI only increases fabrication complexity.

How Is a 14-Layer HDI PCB Stackup Designed?

A 14 layer PCB stackup should be built around routing, impedance, power distribution, board thickness, and via structure.

The HDI PCB stackup must be reviewed with the approved laminate system, finished thickness, copper distribution, and impedance targets before routing is released.

For a broader explanation of layer planning, see our PCB board stackup guide.

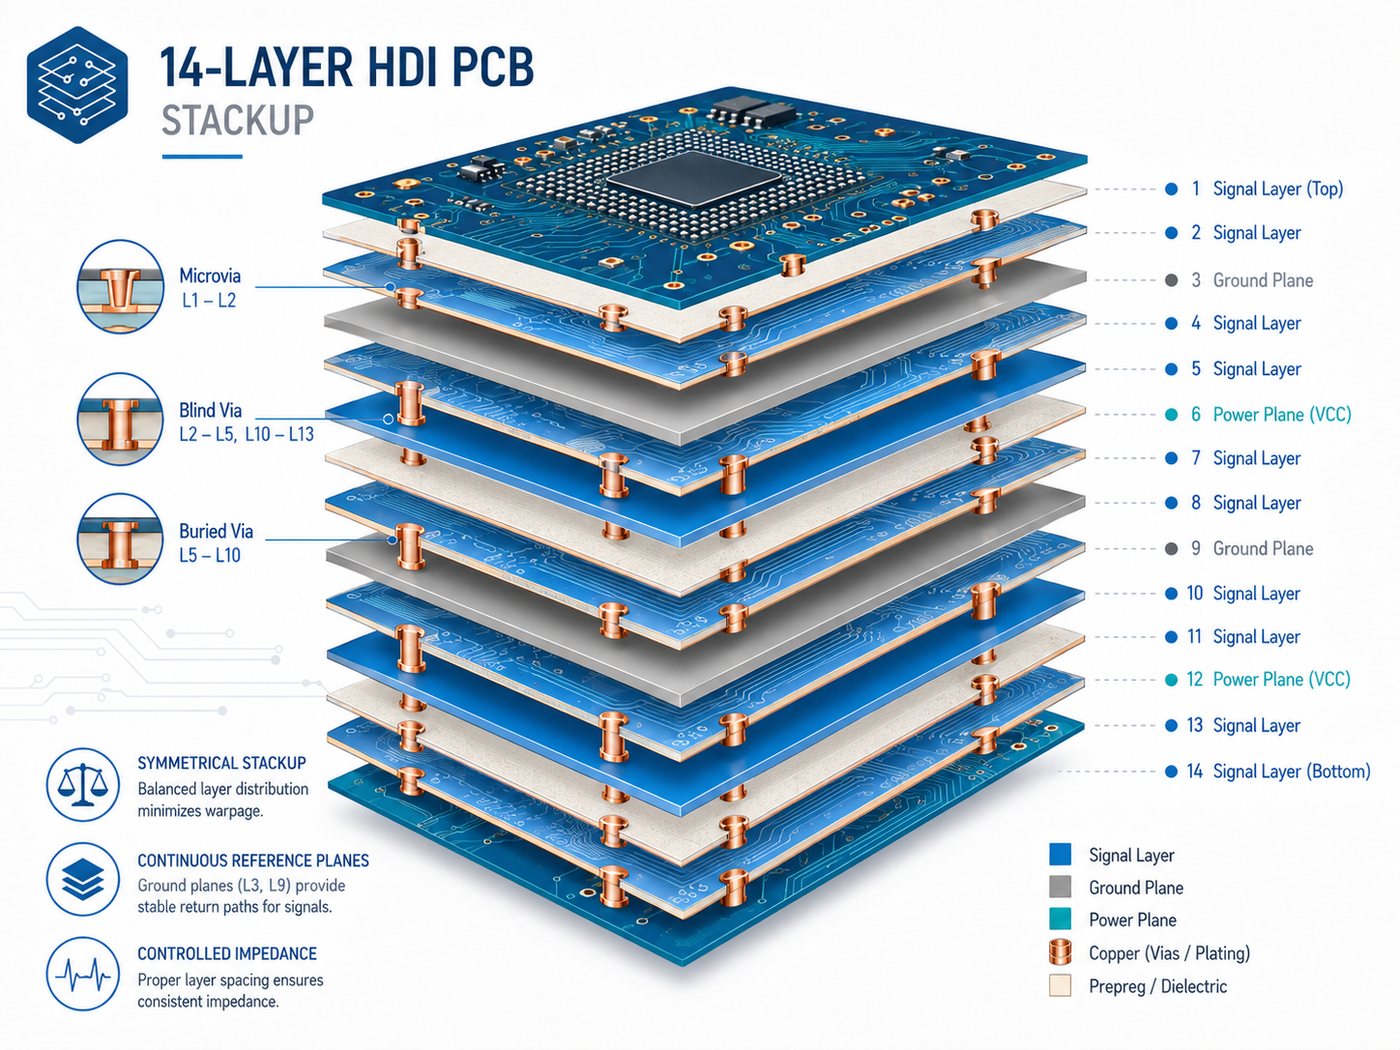
Exploded 14-layer HDI PCB stackup showing signal layers, ground planes, power planes, microvias and blind vias

One possible arrangement is:

Layer Typical Function
L1 Components / high-speed signal
L2 Ground
L3 High-speed signal
L4 Ground
L5 Signal
L6 Power
L7 Ground
L8 Ground
L9 Power
L10 Signal
L11 Ground
L12 High-speed signal
L13 Ground
L14 Components / signal

This is an example, not a universal stackup. Actual dielectric thickness, copper weight, and layer assignment depend on the design.

Three practical rules are useful:

  • Keep high-speed signal layers next to continuous reference planes.
  • Maintain a reasonably symmetrical construction to reduce warpage risk.
  • Define the HDI layer stackup together with the microvia structure.

For example, if microvias connect L1-L2 and L2-L3, the dielectric thickness between those layers must suit the selected laser-via geometry. Stackup review should therefore happen before final routing.

Which HDI Buildup Structure Should a 14-Layer PCB Use?

The buildup defines how many HDI layers are added around the central multilayer structure.

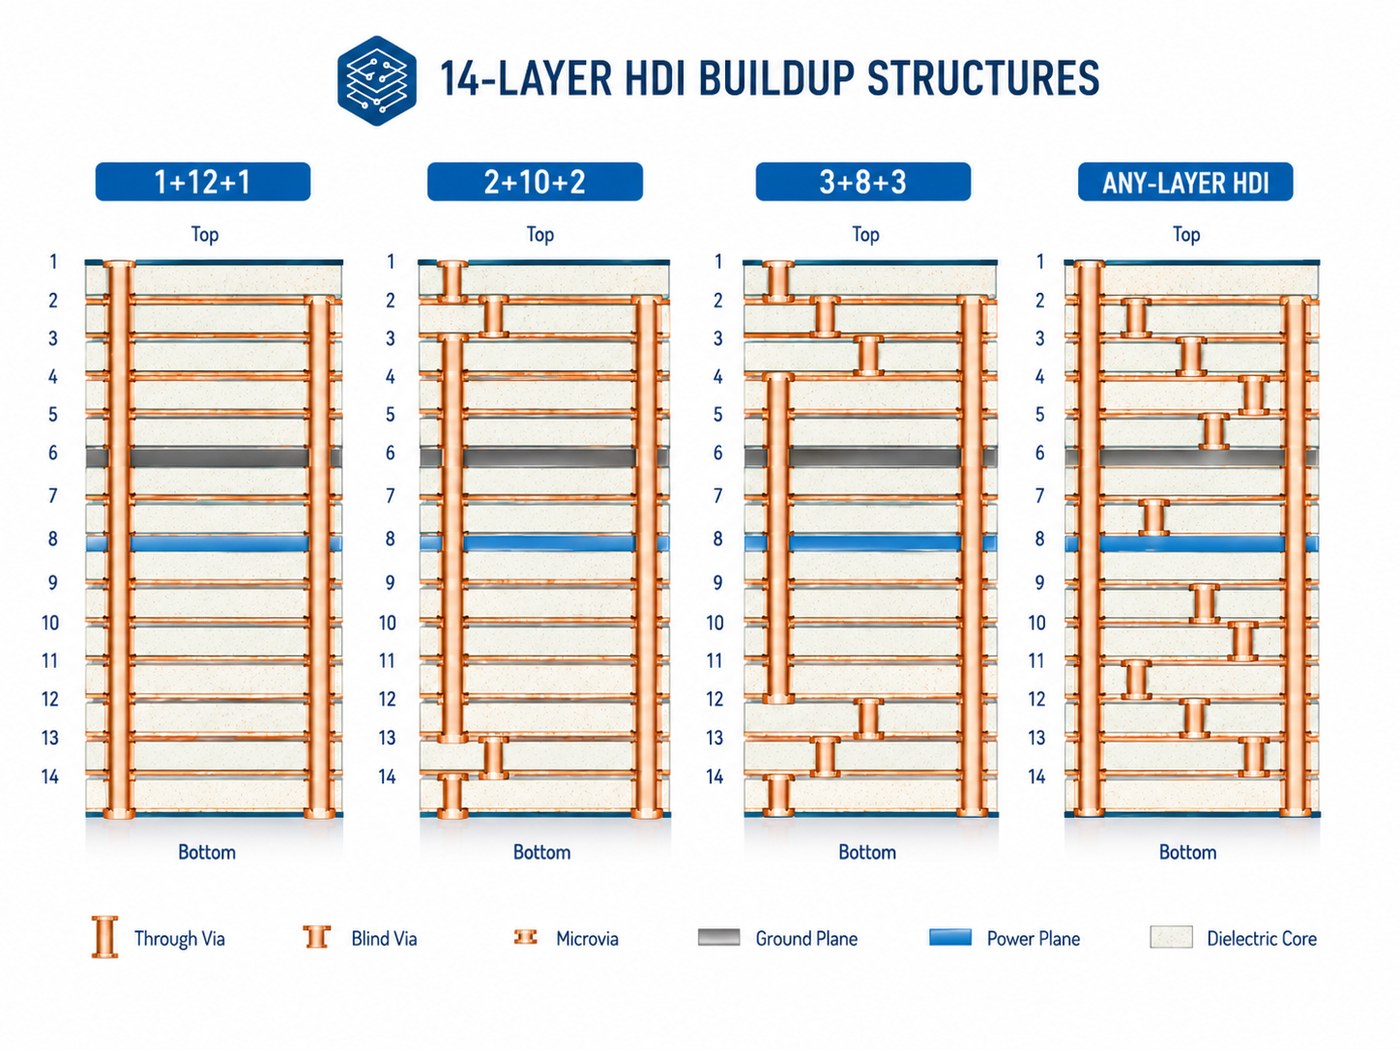
Comparison of 1+12+1, 2+10+2, 3+8+3 and any-layer HDI buildup structures for a 14-layer PCB
Structure Typical Use
1+12+1 Moderate-density outer-layer breakout
2+10+2 Higher-density BGA routing
3+8+3 Very dense component areas
Any-layer HDI Designs requiring maximum interconnection flexibility

A 1+12+1 structure is suitable when signals mainly need to move from the outer layer into the first internal routing layer.

A 2+10+2 structure provides more routing freedom around dense BGAs or processors.

Moving to 3-step or any-layer HDI should have a clear routing benefit. More buildup stages mean additional lamination, laser drilling, plating, filling, and registration control. The best structure is usually the simplest one that completes the routing without compromising electrical requirements.

How Should Microvias, Blind Vias, and Buried Vias Be Used?

Each via type has a different job.

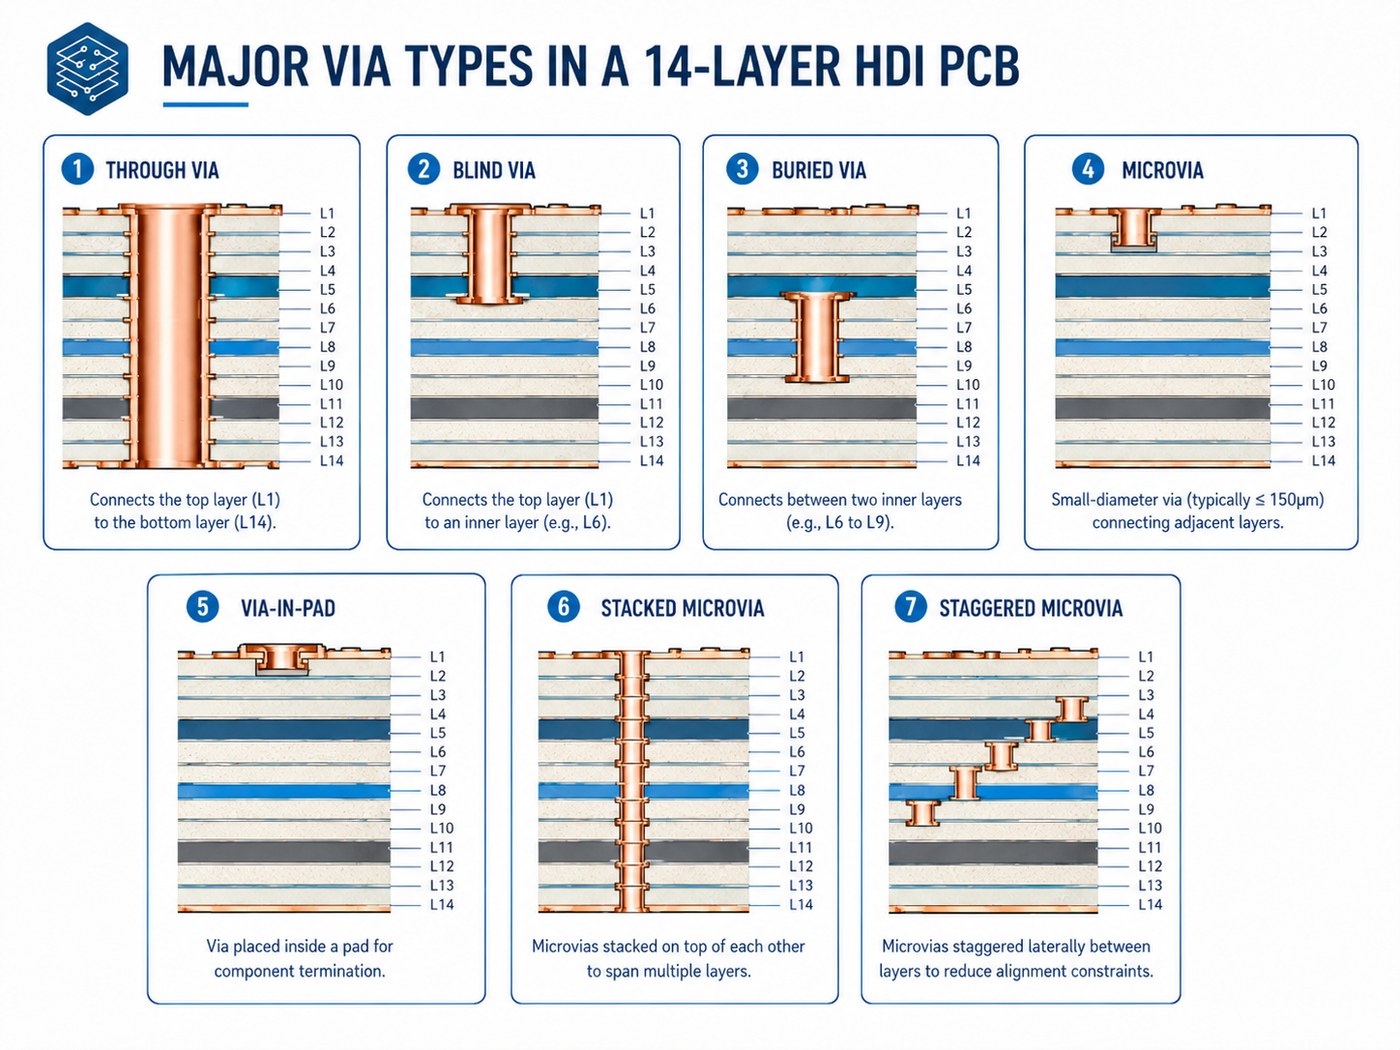
Through via, blind via, buried via, microvia, via-in-pad, stacked microvia and staggered microvia comparison
Via Type Best Use
Through via General connections in lower-density areas
Blind via Outer-to-inner layer connections
Buried via Internal layer-to-layer routing
Microvia Fine-pitch routing between nearby layers
Via-in-pad BGA and small-package breakout
Stacked microvia Maximum routing density
Staggered microvia Multi-level routing where offset space is available

Stacked microvias save space but require tighter control of:

  • Copper filling
  • Layer registration
  • Plating quality
  • Thermal reliability

Staggered microvias are often easier to manufacture when the layout has enough space for an offset transition.

Via-in-pad is useful under fine-pitch BGAs. These vias normally need to be filled and planarized so the component pad remains flat and solderable.

What Are the Key 14-Layer HDI PCB Design Rules?

These HDI PCB design guidelines should match the manufacturer’s actual production capability rather than a generic CAD rule set.

Confirm these items before layout is finalized:

  • Microvia diameter and depth
  • Capture-pad size
  • Annular ring
  • Minimum trace and space
  • Via-to-pad clearance
  • Via filling requirements
  • Stacked microvia capability
  • Layer registration tolerance
  • Controlled impedance

Avoid using the factory’s absolute minimum geometry across the entire board. A feature that can be produced in a small isolated area may not be the best choice for stable volume production.

Copper balance should also be considered across the stack. Large differences in copper distribution between corresponding layers can increase warpage risk.

For controlled impedance, provide the target values and net types. Trace dimensions can then be adjusted against the actual laminate and finished dielectric thickness.

How Do You Control Signal and Power Integrity in a 14-Layer HDI PCB?

Fourteen layers provide useful flexibility for signal and power planning, but only if the reference structure is well organized.

14-layer HDI PCB signal and power integrity illustration with fine-pitch BGA breakout, differential pairs, reference planes and stitching vias

For signal integrity:

  • Route high-speed traces next to solid reference planes.
  • Avoid routing across plane splits.
  • Keep differential-pair geometry consistent.
  • Add nearby ground vias when signals change reference layers.
  • Use short microvia transitions where appropriate.
  • Avoid unnecessary through-via stubs.

For power integrity:

  • Provide low-inductance paths between power and ground.
  • Keep critical power planes close to their return planes where practical.
  • Place decoupling close to high-current and fast-switching devices.
  • Avoid fragmented return paths around plane cutouts.

The benefit of a 14-layer structure is not simply “more layers.” It is the ability to separate routing, reference, and power functions without forcing too many compromises.

Which Materials Are Suitable for a 14-Layer HDI PCB?

Material choice depends on electrical loss, thermal stress, and repeated-lamination requirements.

Material Type Typical Fit
High-Tg FR-4 General industrial HDI
Low-loss FR-4 Higher-speed digital designs
High-performance laminate Demanding thermal or reliability requirements
Hybrid stackup Designs where only selected layers need special properties

Important parameters include:

  • Tg
  • Z-axis CTE
  • Dk
  • Df
  • Resin system
  • Moisture behavior
  • Repeated-lamination performance

For high-speed designs, Dk and Df affect impedance and transmission loss. For multilayer HDI, Z-axis expansion and laminate stability also matter because vias experience repeated thermal stress during fabrication and assembly.

Material availability should be checked before quotation. An uncommon laminate can add unnecessary sourcing time even when the PCB design itself is straightforward.

How Is a 14-Layer HDI PCB Manufactured?

The HDI PCB manufacturing process for a 14-layer board adds sequential buildup steps to conventional multilayer fabrication.

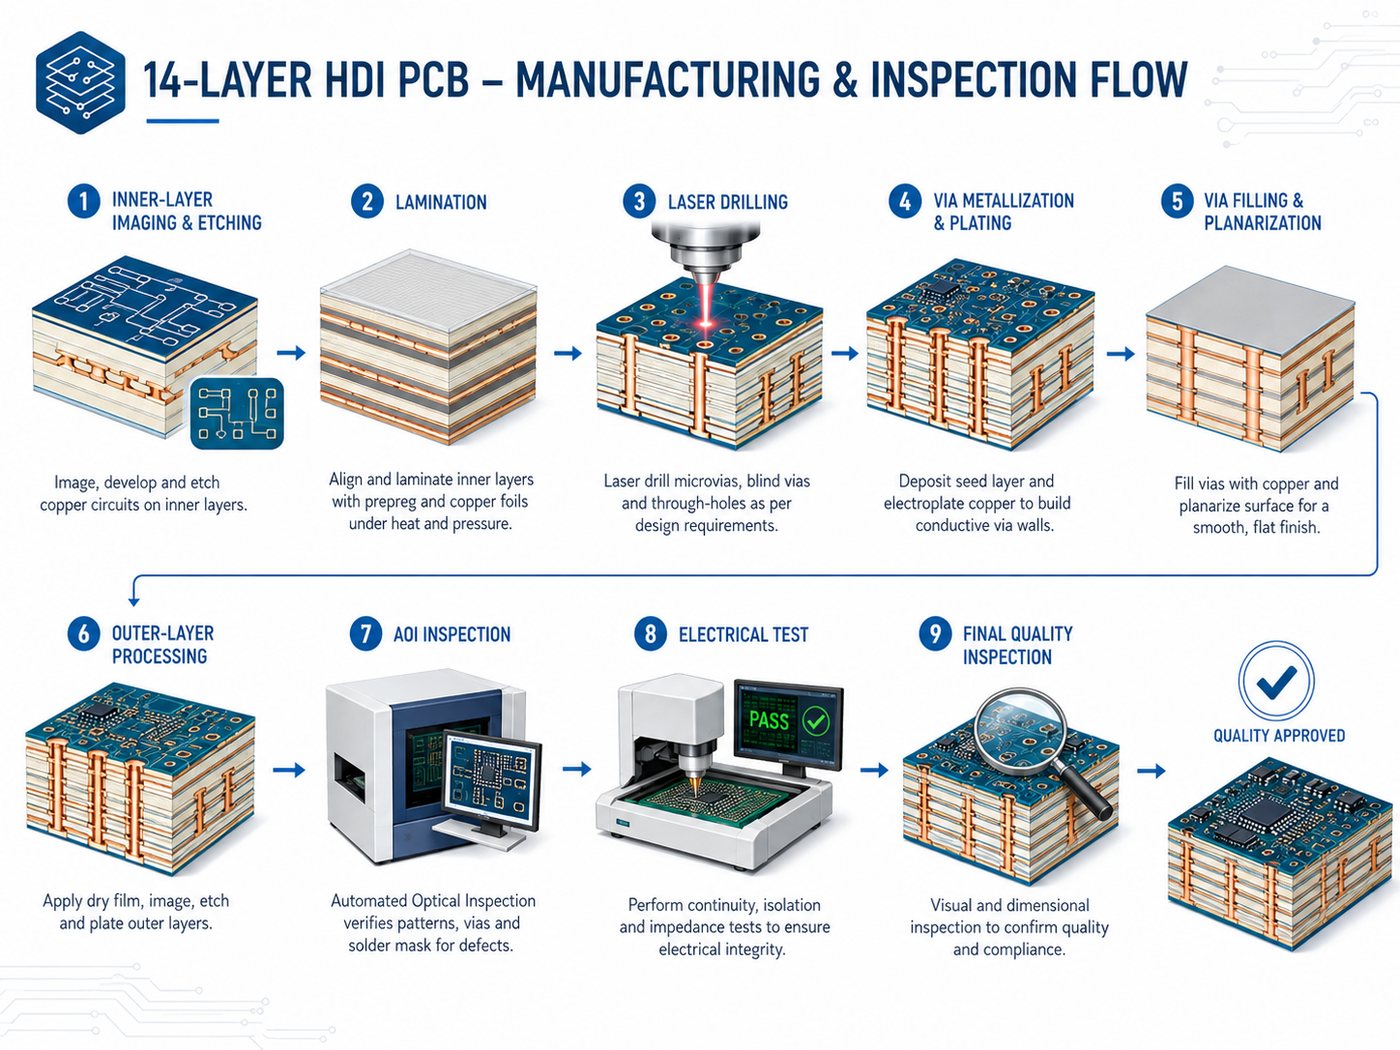
14-layer HDI PCB manufacturing and inspection flow from inner-layer imaging through laser drilling, plating, AOI and electrical test

A simplified flow is:

  • Inner-layer imaging and etching
  • AOI inspection
  • Core lamination
  • Buried-via processing if required
  • Buildup dielectric lamination
  • Laser drilling
  • Via metallization and plating
  • Via filling and planarization where required
  • Additional buildup cycles
  • Outer-layer processing
  • Solder mask and surface finish
  • Electrical and final inspection

A 2+N+2 structure repeats the buildup and laser-drilling sequence for the second HDI level.

The main manufacturing challenge is maintaining alignment and via quality through repeated processing. A factory capable of standard 14-layer PCBs is therefore not automatically qualified for complex HDI builds.

How Is 14-Layer HDI PCB Reliability Verified?

Electrical testing confirms continuity, but HDI also requires inspection of internal interconnects.

Our broader PCB testing guide explains how electrical and inspection methods complement one another.

Method Main Purpose
AOI Conductor and pattern inspection
Electrical test Open and short detection
Microsection Via plating, fill, and registration
Impedance coupon Controlled impedance verification
X-ray Selected internal structure inspection
Thermal testing Interconnect behavior under temperature stress
Dimensional inspection Alignment and finished geometry

Microsection inspection is particularly useful for stacked or filled microvias because the critical structure is hidden inside the PCB.

For high-reliability projects, define acceptance class, coupon requirements, thermal testing, and reporting requirements at RFQ stage. These items can affect both panel design and quotation.

What Affects 14-Layer HDI PCB Cost and Lead Time?

HDI architecture often affects price more than the difference between conventional multilayer counts.

Cost Driver Why It Matters
Sequential lamination Adds fabrication cycles
Stacked microvias Requires tighter registration and filling control
Fine line/space Reduces process margin
Via-in-pad filling Adds filling and planarization
Specialty laminate Raises material or sourcing cost
Tight impedance Requires engineering and verification
Additional reliability tests Adds inspection and qualification
Small prototype quantity Setup cost is spread over fewer boards

One effective way to control cost is to simplify the via structure.

If a 2+10+2 construction completes the routing, moving to 3+8+3 simply for extra flexibility is usually difficult to justify.

When comparing quotes, make sure each supplier is pricing the same material, stackup, microvia structure, surface finish, and testing requirements.

How Do You Choose a 14-Layer HDI PCB Manufacturer?

Do not qualify a supplier only by checking whether its capability table says “14 layers” or “HDI.”

Confirm the processes that your design actually requires:

  • Sequential lamination
  • Laser-drilled microvias
  • Copper-filled via-in-pad
  • Stacked or staggered microvias
  • Fine line and space
  • Controlled impedance
  • Layer registration
  • Microsection inspection
  • Electrical testing

The manufacturer’s DFM feedback should also be specific. If an engineer suggests changing a stacked microvia to a staggered one, the reason should be clear—whether it is reliability, process margin, cost, or production capability.

For quotation, provide:

  • Gerber or ODB++ data
  • Drill files
  • Preferred stackup, if available
  • Material requirement
  • Finished board thickness
  • Copper weight
  • Impedance requirements
  • Microvia and via-in-pad details
  • Surface finish
  • Test requirements
  • Prototype and production quantities

If the stackup is still open, provide the electrical and mechanical requirements instead.

At EBest Circuit, reviewing the stackup and via structure before layout is locked gives engineers more room to resolve manufacturing issues without forcing major redesign later.

Frequently Asked Questions About 14-Layer HDI PCBs

Is every 14-layer PCB an HDI PCB?

No. Fourteen layers describe the copper-layer count. HDI describes the interconnection technology. A 14-layer board can still be a conventional multilayer PCB.

What is a typical 14-layer HDI PCB stackup?

There is no universal stackup. Structures such as 1+12+1 and 2+10+2 are possible, but the final choice depends on BGA routing, impedance, board thickness, and required HDI layers.

What is the difference between a 14-layer HDI PCB and a standard 14-layer PCB?

A 14-layer HDI PCB uses localized high-density connections such as microvias and blind vias. A standard 14-layer PCB may rely mainly on through vias.

Should stacked or staggered microvias be used in a 14-layer HDI PCB?

Use stacked microvias when routing density requires vertical alignment. Use staggered microvias when enough offset space is available and the design does not require the more compact structure.

What files are required to manufacture a 14-layer HDI PCB?

Provide fabrication and drill data plus the stackup or electrical requirements, material, copper thickness, impedance targets, microvia details, via-fill requirements, surface finish, test requirements, and quantity.

How Can EBest Circuit Support Your 14-Layer HDI PCB Project?

At EBest Circuit, we support HDI PCB stackup review, DFM feedback, controlled impedance, laser-drilled microvias, and multilayer PCB fabrication. Send us your Gerber or ODB++ files, stackup, material, finished thickness, impedance targets, via structure, surface finish, test requirements, and quantities for an engineering review and quotation.

You may also like

HDI PCB Design Review: Stackup, Microvia and DFM Checks
Tuesday, July 21st, 2026

An HDI PCB is ready for fabrication only when its package escape, stackup, microvia structure, materials and release data describe one manufacturable system. The most useful design review does not ask whether each feature works in isolation. It checks whether all of those features can be built, inspected and repeated together.

HDI PCB 3D cutaway with build-up layers, microvias and fine-pitch BGA routing

This guide gives hardware designers, PCB layout engineers, quality teams and buyers a practical release sequence. It starts with the reason for using HDI, follows the design through stackup and microvia decisions, and ends with the evidence and files a fabricator needs before production.

What Is an HDI PCB, and When Does a Design Need It?

An HDI PCB is a high-density interconnect board that uses fine conductors and compact interconnect structures to route more connections within limited space. Laser-drilled microvias, blind or buried vias, via-in-pad and sequential build-up layers are common, but the presence of one feature does not automatically make HDI the right choice.

Use HDI when a measurable constraint cannot be solved cleanly with a conventional multilayer construction. Typical triggers include:

  • A fine-pitch BGA whose inner rows cannot escape through practical mechanically drilled vias.
  • A fixed board outline that leaves too few routing channels for the required nets.
  • A thickness limit that makes a larger conventional layer count unsuitable.
  • Critical connections that benefit from shorter stubs or more controlled layer transitions.

If standard through vias, sensible trace rules and an ordinary multilayer stackup can complete the design, HDI may add lamination cycles and process risk without adding product value.

Design condition Likely direction Question to close
Fine-pitch BGA blocks escape channels Evaluate HDI Which pin rows require microvia transitions?
Moderate density and enough board area Keep a conventional multilayer option open Can through vias finish the routing with margin?
Strict thickness or form-factor limit Compare build-up alternatives Can the dielectric and copper system meet the envelope?
HDI has no defined routing benefit Stop and simplify What specific constraint does HDI solve?

What Should Be Defined Before HDI PCB Design Begins?

The component field and electrical constraints should be defined before the stackup is frozen. Starting with a familiar build-up recipe can force the design into unnecessary microvia levels or leave critical BGA rows without a valid escape path.

Prepare a short constraint map that records:

  • BGA pitch, pad size, pin-row count and permitted fan-out direction.
  • Signal groups, differential pairs, clocks and sensitive analog nodes.
  • Power and ground pin distribution, current demand and thermal paths.
  • Board outline, connector positions, keepouts and mechanical height limits.
  • Target finished thickness, copper needs and controlled-impedance nets.
  • Whether via-in-pad is necessary or dog-bone fan-out remains practical.

Route a representative dense area before committing the complete board. This early escape study shows how many build-up layers are genuinely needed and whether placement changes could remove an entire lamination cycle.

How Should an HDI PCB Stackup Be Reviewed?

An HDI PCB stackup should be reviewed as a layer-by-layer connection map, not as shorthand alone. Labels such as 1+N+1 or 2+N+2 describe the number of outer build-up layers, but they do not define dielectric materials, copper thickness, via spans or finished-board tolerances.

Read the proposed construction from the outside inward and confirm every copper layer, dielectric, core, microvia span, buried structure and lamination stage.

Review item What should be confirmed Why it matters
Build-up layers Each added layer solves a documented routing or connection need Unnecessary cycles add cost and registration interfaces
Dielectrics Material family, thickness and resin behavior are agreed They influence laser drilling, lamination and impedance
Copper Base and finished copper are identified by layer Trace geometry and plating allowances depend on copper condition
Reference planes Critical signals keep a continuous return path Plane changes can create return discontinuities
Via spans Every laser, buried and through-hole span matches the construction Ambiguous spans cause CAM questions or invalid connections
Finished thickness Nominal thickness and tolerance include the complete build Core values alone do not define the finished board

Ask the fabricator to return a proposed production stackup before final impedance routing. A late dielectric substitution can change the required trace width, spacing and coupling geometry.

HDI PCB stackup cross-section showing build-up dielectrics and adjacent-layer microvias

Which Microvia Structure Should an HDI PCB Use?

An HDI PCB should use the simplest microvia structure that completes the required layer transitions. A single adjacent-layer microvia usually introduces fewer process interfaces than a multi-level stacked structure, while staggered microvias avoid placing several plated interfaces directly above one another.

Stacked microvias can be necessary when escape space is extremely limited, but they require explicit agreement on via filling, target-pad geometry, plating and reliability validation. IPC has warned the electronics industry about latent failures in some complex microvia structures, so a room-temperature continuity test should not be treated as universal proof of long-term reliability.

  • Identify every laser-drilled, mechanically drilled, blind, buried and through-hole feature.
  • State which microvias require filling and capping for via-in-pad assembly.
  • Avoid stacked levels unless the package escape or connection path requires them.
  • Match microvia depth to the selected dielectric and the fabricator’s qualified process.
  • Define coupon and thermal-stress expectations for reliability-sensitive products.

The PCB via types guide provides a broader comparison of through, blind, buried and microvia structures.

What HDI PCB Design Guidelines Should Be Confirmed with the Fabricator?

HDI PCB design guidelines should be confirmed for the actual material, copper condition, layer role and via process. A generic minimum-rule table cannot show how several difficult features interact in one design.

Close these items before final routing:

  • Trace width and spacing by layer and copper thickness.
  • Laser via diameter, target pad, capture pad and permitted depth.
  • Via-to-copper, via-to-via and via-to-edge clearances.
  • Annular-ring and registration allowances for mechanically drilled holes.
  • Via-in-pad filling, planarization and surface-finish requirements.
  • Solder-mask definition around fine-pitch component pads.
  • Copper-density and balancing expectations in dense areas.

Do not combine every published minimum in the same location. A layout that simultaneously uses the smallest trace, spacing, pad and most complex via structure can be substantially harder to manufacture than one with a single controlled challenge.

How Should BGA Escape and Layer Transitions Be Planned?

BGA escape should be planned by pin function, routing layer and return-current path. The shortest geometric route is not necessarily the best electrical route if a layer transition leaves the signal without a nearby reference connection.

  • Assign outer rows, inner rows, power pins and ground pins before detailed fan-out.
  • Keep critical nets referenced to continuous planes where practical.
  • Place an intentional return path near signals that change reference planes.
  • Maintain differential-pair symmetry through the pad and via field.
  • Review antipad patterns for power-plane neck-down and current crowding.
  • Use the proposed production stackup for impedance calculations.

Large processors and FPGAs require a combined signal- and power-integrity review. Dense escape routing may create enough voiding to fragment a plane even when every individual clearance passes the design rules.

Fine-pitch BGA escape routing with microvias and nearby ground return vias on an HDI PCB

How Do Materials, Copper and Thermal Requirements Affect an HDI PCB?

Materials, copper and thermal requirements affect whether the selected build-up can survive fabrication and assembly while meeting electrical performance. Review dielectric thickness, reinforcement, resin behavior, copper profile and finished copper as a coordinated material set.

A lower-loss laminate is not automatically the best option for every HDI layer. The material must also support laser drilling, resin removal, copper adhesion and the planned lamination sequence. Hybrid constructions need additional attention because different material families may move differently during processing.

Thermal analysis should distinguish signal microvias from deliberate heat-transfer structures. Check how heat moves from component pads into planes, filled thermal vias, copper areas, heat spreaders and the enclosure. Do not assume that a dense field of small electrical microvias replaces a designed thermal path.

How Does the HDI PCB Manufacturing Process Affect Design Decisions?

The HDI PCB manufacturing process affects design because each build-up level adds drilling, metallization, imaging, lamination and registration work. The exact route depends on the via map and layer sequence, so the drawing must describe the construction rather than simply state “HDI.”

  1. Fabricate and inspect the inner core or sub-composite.
  2. Create buried interconnects that must be completed before the next lamination.
  3. Laminate the next dielectric and copper layer.
  4. Laser-drill the specified microvias and prepare the hole surfaces.
  5. Metallize, plate and fill the vias required by the design.
  6. Image and etch the added circuit layer.
  7. Repeat the build-up sequence when more HDI levels are necessary.
  8. Complete outer-layer processing, solder mask, surface finish and profiling.
  9. Perform electrical testing and the agreed inspection or coupon evaluation.

Each repeated cycle creates another opportunity for dimensional movement and registration error. A design that removes an unnecessary build-up level can improve manufacturability without changing the product function.

What DFM Evidence and Quality Data Should Be Reviewed?

A useful DFM review should return specific findings tied to the artwork, stackup and via structure. A generic pass/fail message does not show whether manufacturing assumptions match the design intent.

  • Confirm the production stackup and impedance construction returned by CAM.
  • Review separate drill information for laser, blind, buried and through structures.
  • Check target pads, capture pads, annular rings and solder-mask findings.
  • Review local copper density, plane clearances and copper balancing.
  • Agree on test coupons, microsection locations and acceptance criteria.
  • Define electrical-test coverage and any resistance-monitoring requirement.
  • Record approved exceptions so prototype and production use the same decision basis.

IPC-6012F covers qualification and performance requirements for rigid printed boards and gives expanded attention to microvia structures. The applicable class, revision, customer specification and acceptance plan should be stated in the procurement documentation rather than assumed.

Use the broader PCB design for manufacturability checklist alongside this HDI-specific review.

Laboratory microsection inspection of plated and filled HDI PCB microvias

Which HDI PCB Risks Should Stop a Production Release?

A production release should stop whenever the construction cannot be described unambiguously or a risk spans design, fabrication and assembly. Resolving these issues before quotation is usually faster than answering repeated CAM questions after purchase order release.

Stop condition Likely consequence Required correction
A microvia span does not match the stackup Invalid or unintended layer connection Correct the via map and drill data
Stacked microvias have no validation plan Latent interface risk may be missed Review the structure, coupons and stress criteria
Impedance uses a placeholder dielectric Production geometry changes after routing Approve the proposed material stackup first
Fine-pitch pads conflict with mask capability Missing mask dams or exposed copper Review pad definition with fabrication and assembly
A dense via field fragments a power plane Higher path impedance or local current crowding Rework the fan-out and plane copper
The drawing says only “HDI” Filling, lamination and acceptance remain undefined Add explicit construction and process notes

What Files Should Be Included in an HDI PCB Release Package?

An HDI PCB release package should allow the fabricator to reconstruct the intended build without guessing from artwork. Use one revision across the manufacturing data, drawings and supporting notes.

  • Gerber, ODB++ or IPC-2581 manufacturing data.
  • NC drill files separated by drill type where appropriate.
  • A complete layer stackup with dielectric, copper and finished-thickness requirements.
  • A via map showing every blind, buried, microvia and through-hole span.
  • A fabrication drawing with dimensions, tolerances, finish and acceptance notes.
  • An impedance table tied to layer numbers and net classes.
  • A netlist or other data required for electrical testing.
  • A release readme that identifies the authoritative revision and approved exceptions.

For assembly quotation, include the BOM, centroid or pick-and-place file, assembly drawings, special process notes and expected quantity. Fabrication and assembly data must refer to the same board revision.

How Should an HDI PCB Design Review Checklist Be Used?

An HDI PCB design review checklist should be used as a release gate, not as paperwork completed after the files are sent. Assign an owner to every open item and do not release production data until the construction-critical questions are closed.

Review area Release requirement
Need for HDI The design documents which routing, size or electrical constraint requires HDI
Package escape BGA fan-out, power pins and return paths have been reviewed together
Stackup The material set, build-up sequence and finished thickness are approved
Microvias Spans, filling, stacking and pad geometry are explicit
Design rules Trace, spacing, pad, mask and clearance rules match the selected process
Electrical behavior Impedance and power-integrity work use the proposed production stackup
Reliability Applicable requirements, coupons and inspection criteria are agreed
Release data Artwork, drills, drawings, netlist and revision notes are complete
DFM closure Every CAM exception has an owner and recorded disposition

What Questions Do Engineers and Buyers Ask About HDI PCB?

Is every fine-pitch BGA board an HDI PCB?

No. Package pitch is only one input. Pin-row count, board area, layer availability, pad geometry and routing demand determine whether microvias or sequential build-up layers are necessary. Complete a representative escape study before selecting the construction.

What is the difference between HDI and a conventional multilayer PCB?

A conventional multilayer board commonly relies on mechanically drilled through holes and a simpler lamination route. HDI uses finer interconnect features, often including laser microvias and sequential build-up layers. The practical difference is routing density and process complexity, not layer count alone.

Does an HDI PCB always cost more?

Its fabrication route is usually more complex, but the product-level comparison depends on the design. HDI may reduce board area or avoid additional conventional layers. Compare the complete board, assembly and reliability plan rather than applying one price multiplier.

Are staggered microvias always preferable to stacked microvias?

Staggered microvias are often preferred when space allows because they avoid a direct vertical stack of plated interfaces. Stacked microvias remain useful for very dense connections, but filling, plating and reliability validation require closer control.

When should via-in-pad be used?

Use via-in-pad when component pitch leaves no practical space for dog-bone fan-out or when a short electrical or thermal path is required. The fabrication drawing should define filling and capping so the assembled pad remains flat and solderable.

Can the impedance stackup be finalized after routing?

It should be coordinated before final routing. Production dielectric thickness, copper thickness and copper profile affect the required geometry. A late stackup change may force trace-width and spacing revisions across the board.

Which standards are commonly referenced for HDI design and acceptance?

IPC-2226 is commonly referenced for HDI design, while the IPC-6012 family addresses qualification and performance requirements for rigid printed boards. Purchase documents should identify the applicable revision, class, addenda and customer-specific requirements.

How should microvia reliability be verified?

The plan depends on product risk and via structure. Electrical testing, microsection evaluation, test coupons and thermal-stress or reflow-simulation methods may be appropriate. Complex stacked structures should be reviewed with the fabricator and customer before acceptance criteria are frozen.

What causes the most HDI PCB quotation delays?

Ambiguous stackups, missing via-span definitions, conflicting drill tables, undefined via filling, incomplete impedance information and mismatched file revisions are common causes. A single release readme and clear via map prevent many avoidable questions.

Should prototype and production HDI boards use the same construction?

Use the same critical stackup, via architecture and acceptance basis when the prototype is intended to validate production behavior. A simplified prototype may confirm circuit function, but it cannot validate a different production interconnect structure.

How Can EBest Circuit Review Your HDI PCB Before Fabrication?

Begin with a complete stackup, via map and manufacturing dataset. EBest Circuit can review HDI PCB data for stackup feasibility, microvia structure, impedance requirements and fabrication questions. Send the Gerber or ODB++ package, fabrication drawing, target thickness, quantity and application requirements through the BestPCBs contact page for engineering review and quotation.

You may also like

HDI PCB
Wednesday, April 8th, 2026

HDI PCB, or High Density Interconnect printed circuit board, is built for electronic products that demand more routing space, finer features, smaller vias, and higher circuit density in a limited footprint. Compared with conventional PCB structures, HDI boards support finer lines and spaces, smaller capture pads, and more interconnections per unit area, making them ideal for compact, lightweight, and high-speed devices.

At Best Technology, we provide standard HDI PCB, HDI flex PCB, 2–16 layer HDI multilayer PCB, any-layer HDI PCB, rigid-flex PCB, and high-frequency PCB solutions for customers who need reliable performance, stable manufacturing, and fast turnaround. Our uploaded source also states a monthly production capacity of 260,000 square feet (28,900 square meters), with expedited service available for urgent projects.

What Is HDI PCB?

HDI PCB is the abbreviation of High Density Interconnect PCB. It is a printed circuit board designed with high integration, high precision, and miniaturized interconnection structures. HDI technology uses advanced processes such as microvia formation, via filling, and metallized interconnection to achieve reliable signal transmission and dense circuit routing.

In practical terms, HDI PCB helps designers place more functions into a smaller board area. This makes it a preferred solution for modern electronics that require smaller product size, lighter weight, faster data transfer, and improved electrical performance. The source material describes HDI boards as having finer lines and spaces below 100 μm, smaller vias below 150 μm, and smaller capture pads below 400 μm than conventional PCB technology.

HDI PCB

Why Choose HDI PCB?

HDI PCB is widely used because it gives engineers more design freedom without sacrificing reliability.

Higher Circuit Density

HDI boards use tighter routing, smaller line width and spacing, and more advanced via structures. This allows more components and more functions to fit into the same board outline.

Better Signal Performance

Shorter signal paths and lower impedance help reduce signal delay and transmission loss. This is especially valuable in high-speed digital and high-frequency electronic applications.

Smaller and Lighter Product Design

HDI construction supports thinner, lighter, and more compact products. It is well suited to the ongoing trend toward portable and space-saving electronics.

Strong Reliability

With precise layer buildup, microvia structures, and better interlayer support, HDI boards can provide stable electrical performance and dependable mechanical structure in demanding assemblies.

Our HDI PCB Capabilities

We support a wide range of HDI PCB manufacturing solutions for both prototype and production requirements, including:

ItemCapability
Layer Count2–16 Layers (HDI), Any-Layer HDI Available
Min Line Width / Space3/3 mil (HDI)
Min Via Size~4 mil (Laser Microvia)
Via TypeBlind, Buried, Microvia, Via-in-Pad
Copper Thickness0.5 oz – 3 oz
Surface FinishENIG, ENEPIG, OSP, HASL, Immersion Silver
Board Thickness0.2 mm – 3.2 mm
BGA CapabilityDown to 0.3–0.4 mm pitch
Material OptionsFR4, High-Tg, Low Dk/Df, Polyimide
Max Panel SizeUp to 1200 mm × 360 mm
TestingAOI, X-Ray, Flying Probe, ICT

We also support fast-response manufacturing for urgent orders. According to the provided content, urgent boards can be shipped within 24 hours under suitable project conditions.

HDI PCB Types

According to layer up different, currently DHI board is divided into three basic types:

1) HDI PCB (1+N+1)

HDI PCB (1+N+1)

Features:

  • Suitable for BGA with lower I/O counts
  • Fine line, microvia and registration technologies capable of 0.4 mm ball pitch
  • Qualified material and surface treatment for Lead-free process
  • Excellent mounting stability and reliability
  • Copper filled via

Application: Cell phone, UMPC, MP3 Player, PMP, GPS, Memory Card

2) HDI PCB (2+N+2)

HDI PCB (2+N+2)

Features:

  • Suitable for BGA with smaller ball pitch and higher I/O counts
  • Increase routing density in complicated design
  • Thin board capabilities
  • Lower Dk / Df material enables better signal transmission performance
  • Copper filled via

Application: Cell phone, PDA, UMPC, Portable game console, DSC, Camcorder

3) ELIC (Every Layer Interconnection)

ELIC (Every Layer Interconnection)

Features:

  • Every layer via structure maximizes design freedom
  • Copper filled via provides better reliability
  • Superior electrical characteristics
  • Cu bump and metal paste technologies for very thin board

Application: Cell phone, UMPC, MP3, PMP, GPS, Memory card.

What is HDI Material?

1. Substrate

The substrate is the basis of HDI PCB. Commonly used organic insulating materials include thermosetting resins (such as phenolic resins and epoxy resins) and thermoplastic polyesters (such as polyimide and polytetrafluoroethylene). The choice of substrate depends on the needs of specific applications, such as rigid or flexible PCBs.

2. Copper foil

As a conductive material, the thickness of copper foil is generally between 0.3mil-3mil. The specific choice depends on the current carrying size and etching accuracy. The quality of copper foil directly affects the surface quality and electrical performance of the product.

3. PP (B-stage resin)

When making multi-layer PCBs, PP is an indispensable material as an interlayer adhesive.

4. Photosensitive materials

Including photoresists and photosensitive films, divided into wet films and dry films. These materials will undergo chemical changes under light of a specific wavelength, affecting their solubility in the developer, thereby achieving precise production of circuits.

5. Solder mask (ink)

As a solder mask, solder mask is used to prevent the adhesion of liquid solder, and its performance affects the welding quality and circuit protection of PCBs.

6. Film

Similar to the polyester film used for photography, the film is used to record image data and requires high contrast, sensitivity and resolution while ensuring fine lines and dimensional stability.

HDI PCB Manufacturing Process

The uploaded source outlines a typical HDI PCB manufacturing flow, covering the core steps from design to final inspection.

1. Design Review – define the circuit structure, layer count, and stackup

2. Material Preparation – prepare substrate, copper-clad material, covering layers, and inner layers

3. Laser Drilling – create small vias for interlayer electrical connection

4. Lamination – press the inner and outer layers into a stable structure

5. Etching – remove excess copper and keep the required conductive pattern

6. Plating – improve conductivity and oxidation resistance

7. Assembly – insert and solder components if assembly service is included

8. Testing and Inspection – verify quality and electrical performance

Typical Applications

HDI PCB is widely used in products that require compact design and high functional density. The original material lists applications such as:

  • Cell Phones
  • UMPC
  • PDA
  • GPS Devices
  • Memory Cards
  • Portable Game Consoles
  • Digital Cameras
  • Camcorders
  • Notebook Computers
  • Network Communication Equipment
  • Chip Carriers for Large-Scale IC Packaging

Why Work With EBest Circuit?

We position HDI PCB service around what engineering teams and sourcing teams actually need: broad process coverage, quick response, stable quality, and one-stop manufacturing support. The source content also highlights experience in high-end HDI, multilayer PCB, high-frequency PCB, high-speed PCB, FPC, rigid-flex PCB, SMT processing, and PCBA OEM service.

What You Can Expect

  • Wide HDI product range
  • Prototype to production support
  • Fast turnaround for urgent projects
  • One-stop PCB and PCBA service
  • Competitive pricing with manufacturing support

FAQs About HDI PCB

1. What is the difference between HDI PCB and standard PCB?

HDI PCB uses finer lines, smaller vias, and higher connection density, allowing more circuits in less space compared to standard PCB.

2. When should I use HDI PCB?

HDI is recommended when your design includes fine-pitch BGA, high-speed signals, or strict space constraints.

3. Is HDI PCB more expensive?

Yes, due to more complex processes and tighter tolerances. However, it can reduce overall system size and improve performance.

4. What is the minimum via size in HDI PCB?

Typically around 4 mil (laser drilled microvia), depending on manufacturer capability.

5. Can HDI PCB improve signal integrity?

Yes. Shorter routing paths and better layer control can improve signal performance in high-speed designs.

6. How long does HDI PCB manufacturing take?

Prototype lead time can be as fast as 24 hours, while standard production depends on complexity and volume.

Get a Quote for Your HDI PCB Project

If your project requires microvias, fine-pitch BGA routing, higher wiring density, or compact multilayer construction, HDI PCB may be the right solution. A well-designed HDI board can help reduce product size, improve routing efficiency, and support stronger electrical performance in advanced electronics.

Send us your Gerber files, stackup requirements, and project specifications. Our team can review your design and recommend a suitable HDI PCB manufacturing solution.

You may also like