PCB manufacturing PCB manufacturing
Home > Blog

Blind and Buried Vias

What Is Sequential Lamination in PCB and How Does It Work?
Thursday, September 17th, 2026

Sequential lamination builds a PCB in two or more controlled lamination stages so internal vias can be formed before later layers make them inaccessible. The practical question is not how many layers the board has. It is which blind, buried, or microvia connections must be completed at each stage and what those choices mean for reliability, cost, and lead time.
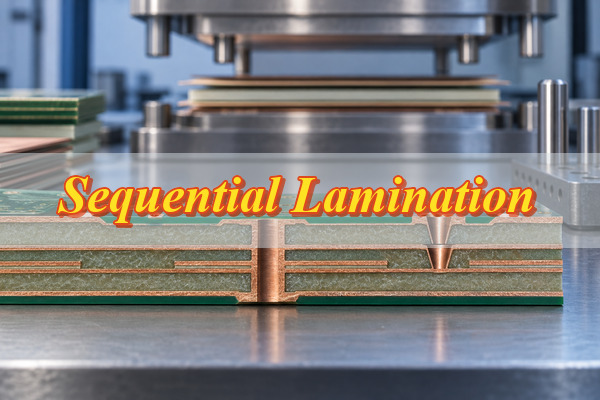
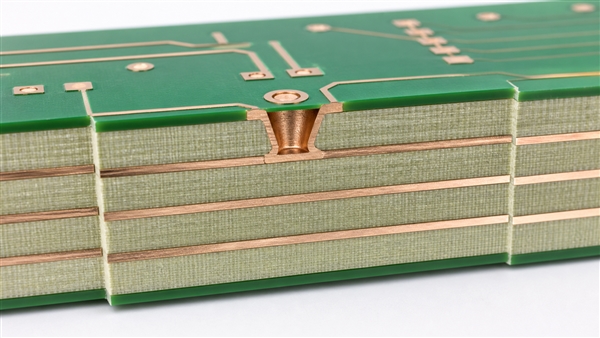
sequential lamination, multilayer PCB cross-section beneath a lamination press

What Is Sequential Lamination in PCB?

A conventional multilayer PCB is usually bonded as one prepared stack. Sequential lamination pauses the build, forms connections in an accessible partial structure, adds another layer set, and continues outward.

A buried via can therefore be drilled and plated before later layers enclose it. Multi-level microvias follow the same logic: each lower tier is completed before the next dielectric covers its landing layer.

The deciding test is layer access. Trace every via from its drilling side to its target layer. If that connection can still be formed after the main bond, another build stage may be unnecessary. If the target becomes enclosed first, the stack must be divided into accessible substructures. Sequential lamination is therefore a construction sequence, not a performance grade.

How Is Sequential Lamination Different From Standard PCB Lamination?

The difference is when the internal connections are made. Standard construction completes most internal preparation before one main multilayer bonding stage. Sequential construction inserts drilling, plating, filling, or inspection between bonding stages.

Factor Standard Multilayer Lamination Sequential Lamination
Lamination process Mainly one multilayer bonding stage Two or more controlled build stages
Via structures Mainly through vias and structures accessible after bonding Buried vias, blind vias, and multi-level microvias
Layer access Internal layers become inaccessible after bonding Selected layers remain accessible between stages
Process complexity Lower when it meets the design Higher because controlled operations repeat
Cost and lead time Generally lower Generally higher
Typical use Conventional multilayer PCB HDI and complex internal via structures

A high layer count does not by itself require sequential lamination. A board with many layers and only plated through holes may use a conventional build, while a board with fewer layers but a buried via or several microvia tiers may need staged construction.

When Does a PCB Design Require Sequential Lamination?

Sequential lamination becomes necessary when a required connection cannot be drilled, plated, filled, or verified after the full stack has been bonded. Four design situations commonly create that condition:

  • Buried vias that would be sealed inside the finished stack: the via must be completed in a core or sub-composite while both target layers are still exposed.
  • Multiple HDI build-up layers: each added dielectric can create a new microvia level that must be formed before another layer is added.
  • Stacked or multi-level microvias: the lower microvia usually needs controlled plating, filling, and a planar landing surface before the upper level is built.
  • Fine-pitch BGA escape that cannot reasonably use through vias: adjacent-layer microvias can release routing area, but their start and stop layers determine the build sequence.

High layer count and the HDI label are not sufficient reasons by themselves. Hide the outer layers in the stackup view, add them back in build order, and note where a connection loses access before it is complete. That via map reveals whether staged construction is necessary and whether a routing change could remove a build-up tier.

How Does the Sequential Lamination Process Work?

The process follows the changing access to each via target. It starts with the innermost structure, adds a layer set, completes the connections that are accessible at that point, and repeats only when the stackup requires another tier.
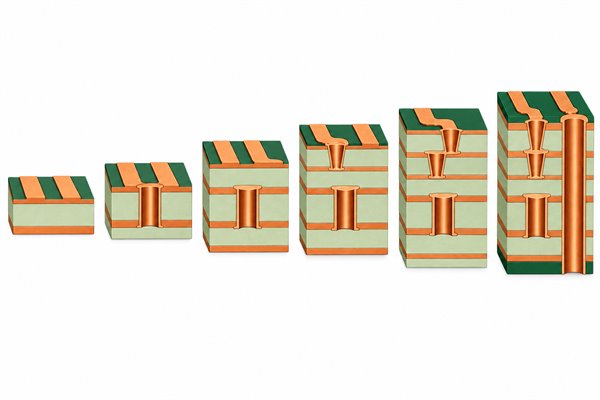
sequential lamination, six-stage PCB build sequence on a white background
  1. Document the stackup and via spans. Identify every copper layer, dielectric, via start and stop layer, fill requirement, and controlled-impedance reference. The output is a build diagram that can be checked before routing is frozen.
  2. Build the initial core or sub-composite. Image and etch the inner copper, then align the partial structure. The layers that will support internal vias remain reachable.
  3. Drill and plate the internal vias. Form the buried holes or first accessible connections, then clean, metallize, fill, and inspect them as required. Their conductive path is complete before enclosure.
  4. Laminate the next layer pair or build-up layer. Add dielectric and copper to the verified partial structure. The result is a larger stack with a new outer surface available for processing.
  5. Form the next blind or microvia level. Drill and plate the newly accessible tier, using filling or planarization where another via must land above it. This completes the next connection level.
  6. Repeat as required and finish the PCB. Continue the add-layer-and-connect sequence for the remaining tiers, then complete final through holes, outer-layer processing, solder mask, finish, profiling, and the agreed testing.

This sequence explains the design consequence: adding or extending one via span can change the required build stages. It may add a fill dependency, alter which layer must remain exposed, or require another controlled cycle.

For the designer, the useful output is a confirmed build diagram: layer order, via levels completed at each stage, landing surfaces required by the next tier, and any geometry or material limit that changes the stackup.

How Do Different Via Structures Affect the Lamination Sequence?

Each via must be formed while its drilling side and target layer are accessible. The name of the via helps describe the connection, but the exact start-stop layers and stacking arrangement determine the sequence.
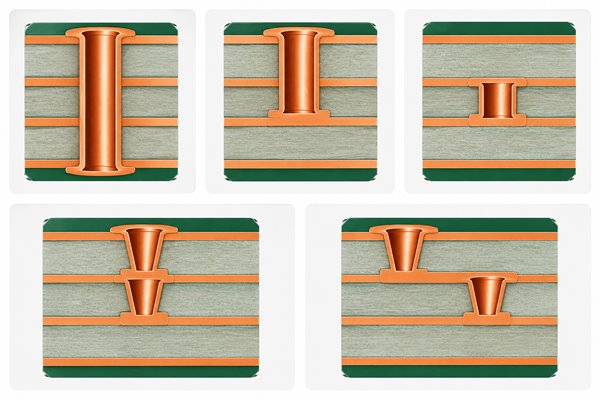
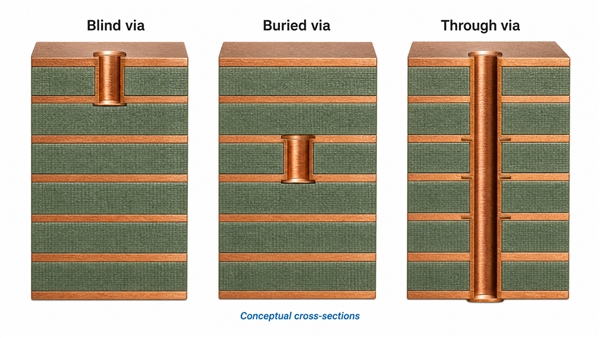
sequential lamination, cross-sections of through blind buried stacked and staggered vias
  • Through vias: these normally pass through the completed stack and can be drilled after final lamination, so they do not create a sequential stage by themselves.
  • Buried vias: these connect internal layers and must be processed before later layers hide both ends.
  • Blind vias: these connect an outer surface to an internal target. Their route depends on the depth, dielectric thickness, drill method, and stage at which the target is exposed.
  • Single-level microvias: these usually connect adjacent layers through a thin dielectric and may fit within one build-up stage.
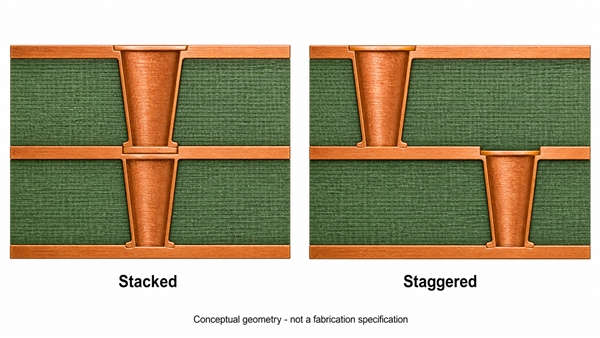
  • Stacked microvias: the upper microvia lands directly above the lower one, creating a fill and planarity dependency between tiers.
  • Staggered microvias: the levels are offset, which avoids a direct via-on-via interface but does not necessarily remove the need to build each dielectric tier in sequence.

Do not assign a cycle count from terms such as blind via or HDI alone. Two boards can use the same via label yet require different sequences because the vias stop on different layers or use different fill and stacking arrangements.

How Does the PCB Stackup Determine the Number of Lamination Cycles?

The cycle count follows the number of connection groups that must be completed before another layer blocks access. Total layer count matters less than the order in which via targets disappear inside the stack.

Notation such as 1+N+1 or 2+N+2 shows the build-up layers around a core region, but it does not prove a universal press count. The core may contain buried vias, and outer tiers may be stacked, staggered, symmetric, or one-sided. The notation shows the layer arrangement; the via start-stop map shows the build dependencies.

Three simplified cases show how that logic changes the build:

  • Eight-layer board with through vias only: the prepared layers can normally be bonded in the main multilayer lamination, followed by through-hole drilling. The layer count does not create another stage by itself.
  • Core containing buried vias: the internal via is drilled and plated while its core or sub-composite is accessible. Outer layers are laminated only after that connection is complete, so the via architecture creates a staged build.
  • 2+N+2 HDI with stacked microvias: the first microvia tier must be formed before the second build-up dielectric covers it. Direct stacking can also require a filled, planar lower via before the upper tier is added.

Estimate the sequence from the inside out:

  1. Map every start and stop layer. Separate through, blind, buried, and microvia spans.
  2. Group connections that are accessible together. Vias that can be formed in the same exposed sub-composite may share a stage.
  3. Mark each covering event. When a new dielectric hides a completed target, record the lamination needed before that happens.
  4. Add stacking dependencies. A microvia tier that needs a filled, planar lower via must be completed before the next tier can begin.

If two proposed builds show different cycle counts, compare their layer-by-layer diagrams, via formation stages, and fill sequence before treating either number as correct.

What Should You Check Before Finalizing a Sequential Lamination Stackup?

Review the stackup before dense routing makes the construction difficult to change. The goal is to prove that every added tier solves a real routing or electrical constraint and that its build dependency is understood.

  • Via start and stop layers: make the CAD data, drill table, and cross-sectional stackup agree.
  • Stacked or staggered arrangement: confirm whether direct stacking is necessary or an offset path can meet routing and reliability needs.
  • Number of build-up tiers: test whether a routing change, another conventional layer, or a different escape pattern can remove a tier.
  • Material system: check whether cores, prepregs, build-up dielectrics, and copper constructions suit the planned press and assembly thermal history.
  • Impedance and reference layers: protect return paths, reference-plane continuity, dielectric targets, and any backdrill requirement when the build changes.
  • Reliability requirements: state the product environment, assembly exposure, acceptance class, coupon needs, and qualification expectations.

Generic online limits should not be copied directly into CAD rules. Usable geometry depends on the material, dielectric thickness, copper, drill and fill process, registration capability, and product requirement. For a useful DFM or quotation review, send the stackup, via map, fabrication data, quantity, and reliability requirements together.

How Can Multiple Lamination Cycles Affect PCB Reliability?

Extra cycles add thermal, pressure, and registration exposure. That does not make a sequentially laminated PCB unreliable by definition, but it reduces the value of judging the design by layer count or a room-temperature electrical test alone.

Risk area Why multiple cycles matter What to verify
Microvia interface Repeated thermal exposure can reveal weak plating, fill, or target-pad interfaces Via structure, fill route, representative coupons, and qualification method
Layer registration Alignment error can accumulate as more structures are bonded Capture pads, registration allowance, and evidence from intermediate stages
Material thermal history The laminate experiences repeated heat and pressure before assembly reflow Material suitability for the full fabrication and assembly history

Risk is often concentrated at interfaces: a microvia base meeting its target pad, a filled via supporting an upper tier, or resin bonding around uneven copper. Residue, voids, weak plating, poor planarity, expansion mismatch, and registration error can reduce margin during reflow or thermal cycling.

Qualification should represent the connections with the greatest structural dependency. Match the coupon or test vehicle to the microvia tiers, target-pad interfaces, fill arrangement, materials, and expected assembly exposure. A room-temperature continuity check confirms a path at that moment; it does not reproduce repeated reflow or service thermal cycling.

How Does Sequential Lamination Affect PCB Cost and Lead Time?

Cost and lead time usually rise because pressing, drilling, plating, filling, planarization, and inspection may repeat for each build stage. There is no reliable universal percentage; the impact depends on the stackup, material, panel use, via density, registration demand, testing, and quantity.

  • Repeated controlled operations: each added tier consumes equipment time and requires another alignment and processing sequence.
  • Fill and planarization: stacked structures may need a prepared landing surface before the next level can be formed.
  • Intermediate verification: hidden circuitry and via quality need to be checked before the next layer removes access.
  • Longer dependency chain: later work cannot begin until the preceding structure is complete and suitable for the next tier.
  • Greater late-stage loss: a defect found after several completed stages affects more accumulated processing than an early defect.

The best cost reduction is often one unnecessary build-up tier removed before layout release. Compare alternatives that preserve the same electrical and mechanical requirements, such as fewer unique via spans, staggered rather than stacked microvias, a different BGA escape, or an added conventional layer.

FAQs About Sequential Lamination Technology

Q1: What files help a supplier quote the actual build instead of making assumptions?

A1: Send one consistent data package. Include Gerber or ODB++ data, NC drill data, a controlled stackup, via start-stop layers, finished copper weights and board thickness, material and impedance requirements, via-fill or cap requirements, acceptance and test expectations, quantity, and target delivery date.

Q2: How should blind and buried via spans appear in the drill data?

A2: Every start-stop layer pair must be unambiguous. Separate drill files or a clearly mapped drill table can be used, but each span should identify its layer pair, plated status, finished size, tolerance, and any fill or cap requirement. The naming convention matters less than agreement between the drill data, stackup, and fabrication drawing.

Q3: Can stacked microvias be changed to staggered microvias without design approval?

A3: No. The alternative may improve the build margin, but it changes pad locations, routing space, and possibly reference-plane or impedance conditions. It should be proposed as a documented DFM change and approved in the controlled design data before production.

Q4: Why can two PCB quotations use different build sequences?

A4: The suppliers may be working from different assumptions or grouping operations differently. Compare the annotated build diagrams, via spans, fill and planarization route, materials, impedance construction, and test scope. A lower cycle number is not automatically the better or equivalent proposal.

Q5: Can an enclosed buried-via defect be repaired after final lamination?

A5: It is generally not a practical local rework. The connection is trapped inside the bonded stack, so opening it can damage surrounding layers and dielectric. Intermediate inspection, representative coupons, and final electrical testing are used to find problems; an affected bare board is usually rejected or rebuilt rather than patched.

Ready to build a sequential-lamination PCB? Send your stackup, Gerber or ODB++ files, via map, material and impedance requirements, quantity, and target delivery date to sales@bestpcbs.com. EBest Circuit can review the proposed construction and prepare a PCB quotation based on the actual build sequence.
You may also like

When Should You Use Blind Vias in HDI PCB Design?
Wednesday, September 2nd, 2026

Blind vias connect an outer copper layer to an internal layer without passing through the entire PCB. Use them when dense component escape routing or an unwanted signal stub creates a problem that ordinary through vias cannot solve efficiently. They can free routing space, but add constraints to drilling, plating, stack-up and inspection. The right choice is the simplest manufacturable interconnection that meets the circuit’s needs.

Conceptual blind vias cutaway showing a shallow copper connection stopping at the first internal layer

What Is a Blind Via?

A blind via is a circuit board via with one end at an external surface and the other at an internal target layer. A blind via hole is therefore accessible from one board face but does not open onto the opposite face. For example, an L1-L2 connection in a six-layer board is blind; an L1-L6 connection is through.

For background, PCB vias are conductive connections between copper layers, not unplated mounting holes. Questions such as “what is a via?” or “what are vias?” concern this basic vias meaning; a blind via adds the condition that the connection stops inside the board.

A blind via PCB can contain other types of vias too. Using blind vias in PCB routing does not mean every connection must be blind. Through vias may remain appropriate for connectors, power distribution or signals needing a different layer span.

The construction is determined by the finished board, not only by the drilling operation. A hole drilled through a subassembly may become blind after additional layers are laminated to that subassembly.

What Is the Difference Between Blind and Buried Vias?

Blind vias and buried vias differ in whether they reach a finished board surface. A buried via connects internal layers only. Its connection must be manufactured while those layers are accessible, before they are enclosed by later lamination.

Connection Finished-board span Useful when Main trade-off
Blind via Outer layer to internal layer Surface component escape needs routing space below Depth, plating and build sequence need review
Buried via Internal layer to internal layer Inner-layer routing should not consume outer pads Hidden interconnects and additional processing
Through via Entire board thickness Conventional routing can tolerate its barrel and clearances Unused barrel may form a stub; occupies more layers

The buried via vs blind via decision follows the required endpoints. A buried via hole cannot directly provide the top-surface connection of a component pad. Conversely, a blind via and buried via may be combined within the same HDI stack-up. These are complementary PCB via types, not competing quality grades.

Blind vias compared with buried and through vias using conceptual PCB cross-sections

Blind Via vs Microvia: Are They Different?

Yes, but the categories overlap. “Blind” describes the layers a connection reaches. “Microvia” describes a small, shallow interconnect structure, commonly laser formed in an HDI build-up layer. A surface-to-next-layer microvia is also a blind via; a mechanically drilled blind connection is not automatically a microvia.

In a microvia PCB, several short connections can be arranged across successive build-up layers. A deeper connection should not be called a microvia merely because its opening looks small. The hole formation process, depth, diameter and applicable qualification requirements must all agree.

The practical answer to microvia vs blind via is therefore not “choose one.” First choose the required layer span, then determine whether a shallow laser microvia or another qualified blind structure can realize it.

When to Use Blind Vias?

Use blind vias when they remove a specific routing or electrical limitation. Common reasons include escaping fine-pitch BGA pads into a nearby routing layer, preserving inner-layer channels, and shortening an otherwise excessive signal-via stub.

  • Dense surface routing: a short L1-L2 connection can move a signal away from a crowded pad field without reserving a through-hole clearance on every layer.
  • Constrained board area: recovering routing space can help when changing the enclosure or connector locations is not practical.
  • Controlled high-speed transitions: a shorter barrel may reduce the unused stub, provided the pad, antipad and return-path geometry are also suitable.

For our HDI printed circuit boards, interconnection planning starts with the component escape pattern and feasible build-up. Adding blind vias after routing is complete can force a stack-up redesign.

In compact rigid-flex circuit boards, dense connections may be needed in a rigid component area while the flexible section carries interconnects between assemblies. Any blind-via option requires construction-specific review. Do not extend a rigid-area via rule into a dynamic bend region or assume a via can sit at a rigid-flex transition without assessment.

Keep conventional through vias when they already satisfy routing, electrical and mechanical requirements. An HDI feature is not automatically an improvement on a simple board.

How Are Blind Vias Made?

The PCB blind via fabrication process depends on when the target layer is accessible. Shallow laser drilling is common for build-up microvias. Controlled-depth mechanical drilling or drilling a subassembly before further lamination can serve other blind structures.

  1. Define the layer pairs, materials and fabrication sequence.
  2. Form the hole to the intended copper target or through the relevant subassembly.
  3. Clean the hole and prepare the dielectric and target-pad surfaces for metallization.
  4. Deposit and build copper to create the electrical connection; fill and planarize when the specified construction requires it.
  5. Complete subsequent imaging and lamination stages, then inspect and electrically test the finished connections.

Via hole drilling is only one operation in that sequence. A correctly located cavity can still fail if residue prevents adhesion at the target pad or copper deposition is inadequate. Blind/buried vias also require clear identification of each drill span; one undifferentiated drill file cannot adequately describe several different layer pairs.

In HDI PCB design, reaching deeper routing layers may require a chain of microvias through successive build-up layers. The outer connection is blind, while connections entirely inside the finished board are buried. These successive microvias can be vertically stacked or laterally staggered, so their arrangement belongs in the fabrication plan rather than being treated as an unrelated hole type.

How Do Stacked Vias Differ from Staggered Vias?

Stacked vias align successive microvias vertically. A stacked via structure saves lateral space, but introduces copper-fill and interfacial requirements at each level. Staggered vias offset successive connections and join them with an intermediate trace or pad region.

A staggered via layout uses more area but can simplify certain interconnect interfaces. Neither arrangement is automatically reliable or unreliable: the number of build-up levels, materials, process control and qualification evidence determine suitability.

The minimum blind buried via stagger distance cannot be selected as one universal number. It depends on capture and target pad diameters, registration tolerance, copper spacing and the manufacturer’s approved construction. Measure the clearance between real copper features, not only between drill centers.

Conceptual stacked and staggered blind vias with separate copper target-pad interfaces

What Blind Via Aspect Ratio Is Practical?

Define the ratio before comparing limits. Here, via aspect ratio = connection depth divided by drilled hole diameter. For a blind connection, use its own depth, not the full finished-board thickness. Some supplier tables express the inverse ratio, so a bare ratio without its definition is ambiguous.

As a geometry example, an 80-micrometer-deep opening with a 100-micrometer diameter has a depth-to-diameter ratio of 0.8:1. This calculation is illustrative, not a production limit. A shallower blind via aspect ratio generally makes cleaning and copper deposition easier, but material, taper, target-pad condition and plating method still matter.

Many laser-microvia processes use shallow geometries around or below 1:1, with the acceptable value set by the qualified fabrication process. Do not apply a general through-hole aspect-ratio capability to laser microvias. A “blind via ratio” requirement must state the dimensions and convention being used.

Finished opening size, drilled diameter and bottom diameter are not interchangeable. For deeper blind structures, consult the actual process limits rather than extrapolating a shallow microvia rule.

What Changes with Blind Via in Pad Designs?

A blind via in pad can provide a short escape route directly beneath a component termination. It also puts the hole treatment and surface condition inside the soldering interface. An open cavity may consume solder or affect joint consistency.

Specify the required filling, planarization and cap treatment for the actual assembly process. A capped via has a copper-covered surface, but that name alone does not describe the complete internal fill structure or guarantee a flat solderable land. Solder-mask tenting is not the same as copper filling and capping.

For fine-pitch pads, evaluate surface depression or protrusion, finish and solder-joint requirements together. Do not assume every PCB blind vias design requires identical filling, or that any filled hole is acceptable beneath any package.

Blind Via vs Backdrill: Which Solves the Problem?

The blind via vs backdrill comparison matters when an unused plated barrel is the main concern. Backdrilling removes an unwanted portion of an already plated through via using a larger controlled-depth drill. It reduces the stub but does not create the same build-up structure as a blind microvia.

A blind connection may also free routing space below its endpoint. A backdrilled hole still needs clearance for the larger drill and a controlled residual stub. If routing space is available and the issue is primarily signal integrity, backdrilling may be worth comparing with an HDI reconstruction.

On RF printed circuit boards, the substrate and complete transition geometry must be reviewed together. A short signal barrel alone does not establish a good RF transition: return connections, pad capacitance, antipads and material behavior remain important. We assess process compatibility for the selected laminate instead of assuming every RF material supports the same blind-via process.

For backdrill vs blind via decisions, compare the modeled transition, remaining stub tolerance, routing impact and fabrication sequence. Do not promise a fixed bandwidth improvement from the via name alone.

Are Blind Vias More Expensive?

Usually, compared with an otherwise similar conventional through-via board. Blind via cost can increase because of laser or depth-controlled drilling, additional lamination stages, copper filling, registration requirements and inspection. The premium is design dependent, not a fixed percentage.

Blind vias cost should also be considered at assembly level. If the construction removes unnecessary layers or enables a substantially smaller board, the system-level result may differ from the price of one fabrication operation. Compare manufacturable alternatives with the same functional requirements.

To control cost, use only the necessary layer spans, favor a repeatable build-up, and avoid specifying maximum density throughout areas that do not need it. Simplifying a stack-up early is usually more useful than trying to negotiate around an unnecessarily complex finished layout.

Which Blind Via Design Rules Should Be Checked?

Blind via design rules for printed circuit board vias must come from the agreed stack-up and fabrication process. A printed circuit board via needs the intended copper connection and isolation from unrelated nets. A CAD rule set is useful only when its assumptions match the intended manufactured structure.

  • Layer span: every via pair must have a feasible drilling and lamination sequence.
  • Depth and diameter: check the stated aspect-ratio convention and the relevant hole dimensions.
  • Capture and target pads: preserve registration allowance and the required copper connection.
  • Clearances: inspect adjacent traces, plane antipads and the actual spacing in dense escape areas.
  • Surface treatment: define fill, cap and flatness where vias share component lands.
  • Return path: ensure the signal transition has an appropriate nearby reference connection.

Our PCB via size guide provides additional terminology context. Its general hole-size discussion does not replace construction-specific blind-via approval.

How Can Blind Via Reliability Be Verified?

Use complementary checks. Electrical testing detects connectivity problems; cross-section inspection examines the physical interconnect. A sample that passes continuity today may still contain an interface weakness that appears after assembly or thermal cycling.

Verification Purpose Boundary
Stack-up and fabrication-data review Confirm layer pairs, pad geometry and process sequence Does not prove physical plating quality
Electrical testing Identify opens and unintended shorts Does not by itself establish fatigue life
Microsection examination Inspect target-pad interface, copper distribution and fill Samples selected locations, not every via
Assembly and thermal-stress qualification Evaluate the selected construction under defined exposure Results apply to the tested conditions and structure

Review misregistration, contamination, copper voids, interface separation and thermomechanical stress as possible failure mechanisms. The appropriate coupon, sample plan and stress profile depend on product requirements. X-ray inspection can complement the process, but not every interface defect is visible in a conventional X-ray image.

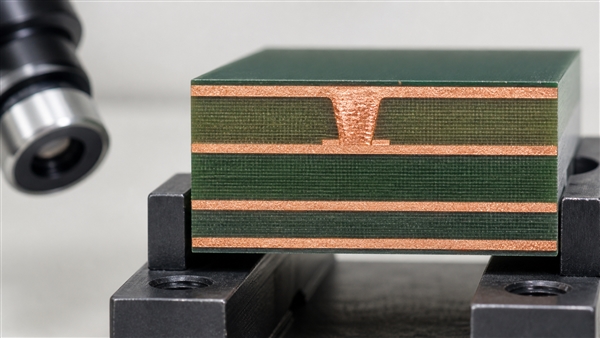
Illustrative blind vias microsection coupon showing copper fill and internal target-pad contact

More Questions About Blind Vias

Can a four-layer PCB use blind vias?

Yes, where an approved stack-up and process support the required layer pair. A four-layer board is not automatically an HDI board, and its layer count alone does not prove that a particular blind via is manufacturable. Compare the routing benefit with the added processing before selecting it.

Can blind vias replace thermal vias?

Not automatically. Thermal vias conduct heat toward a copper region or heat-removal path. A blind connection ending at an internal plane does not by itself carry heat to the opposite surface. Evaluate the complete thermal path, copper area and assembly rather than substituting via names.

What should be checked for Altium blind vias?

For Altium blind vias, define the stack-up and intended drill pairs, apply the fabricator-approved constraints, and inspect the exported manufacturing data. The connections displayed in the layout must correspond to actual, unambiguous layer spans in the output. This is a design review principle, not a version-specific click-by-click tutorial.

What should be checked for KiCad blind vias?

For KiCad blind vias, confirm that the selected board setup and routing rules allow the intended structure, then review the drill outputs with their start and stop layers. A rendered hole in a 3D preview does not confirm its fabrication sequence. Editor behavior and supported options depend on the version being used.

What does skip via vs blind via mean?

A skip via bypasses an intermediate conductor level to reach a deeper target. It may also be blind when it starts at an outer surface. Skipping a layer changes drilling, isolation and plating demands; it is not a way to ignore depth limits. Have the specific construction qualified instead of treating it as an ordinary adjacent-layer microvia.

Our Blind Via PCB Manufacturing Support

At EBest Circuit (Best Technology), we support blind and buried interconnection planning with our HDI manufacturing capability. Our available constructions include 1+N+1, 2+N+2 and 3+N+3 build-ups, with HDI line/space down to 2/2 mil and minimum hole capability down to 0.10 mm, subject to materials, board dimensions, stack-up and engineering review. These limits are not a blanket approval for every layer span, aspect ratio or combined feature set.

We review the proposed construction against our PCB manufacturing capabilities before treating a design as production ready. Our aim is to support the required routing and electrical function with a feasible build sequence, suitable inspection and clearly defined acceptance requirements.

Conclusion

Choose blind vias for a demonstrated routing or transition problem, not simply because the option is available. Define the endpoints, compare conventional and HDI constructions, and review depth, plating, fill and reliability together. For construction and fabrication support, contact our team at sales@bestpcbs.com.

You may also like