PCB manufacturing PCB manufacturing
Home > Blog

Metal Core PCB Material: Aluminum, Copper, Thickness and FR4 Comparison

May 11th, 2026

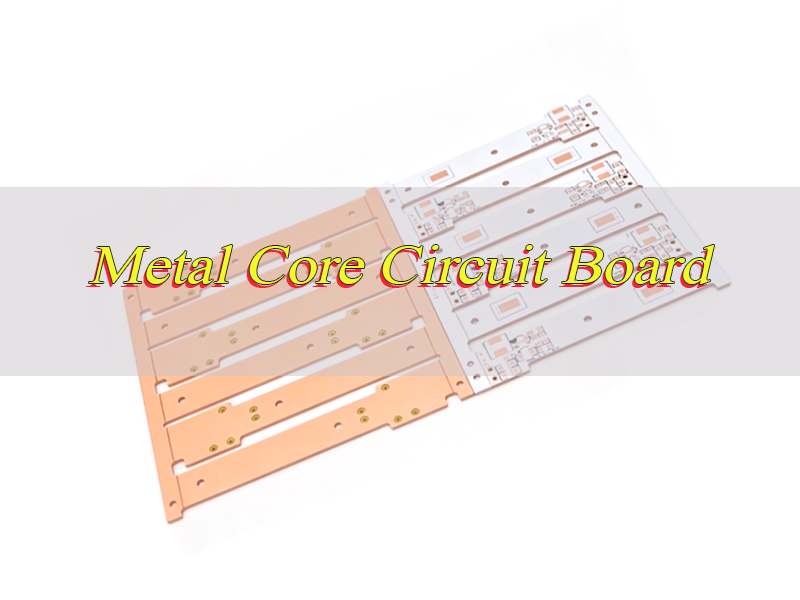
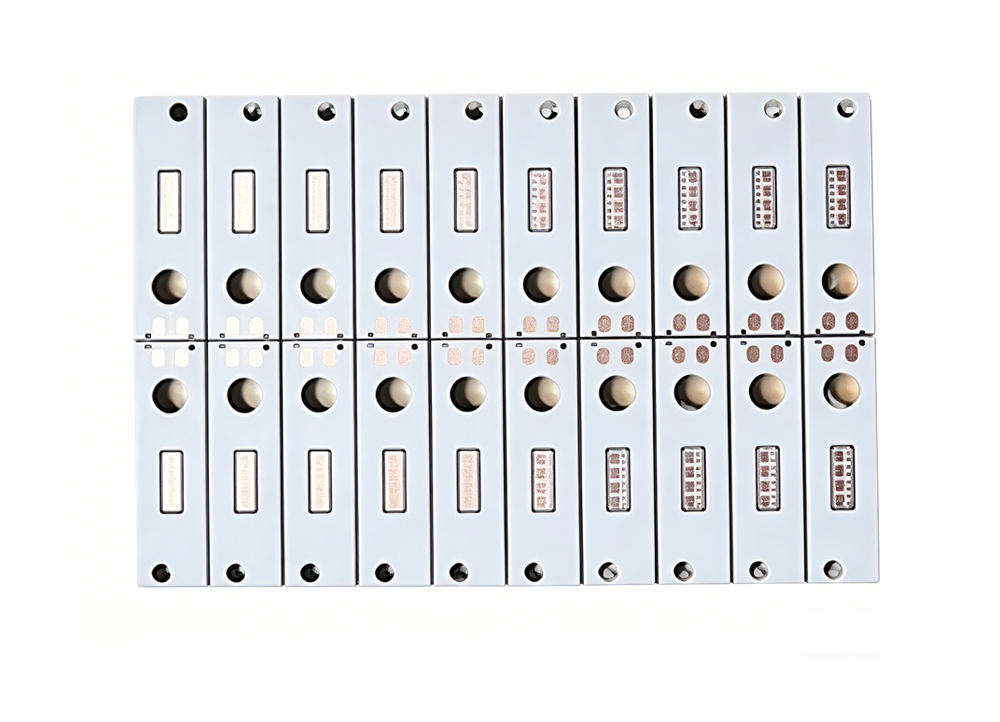
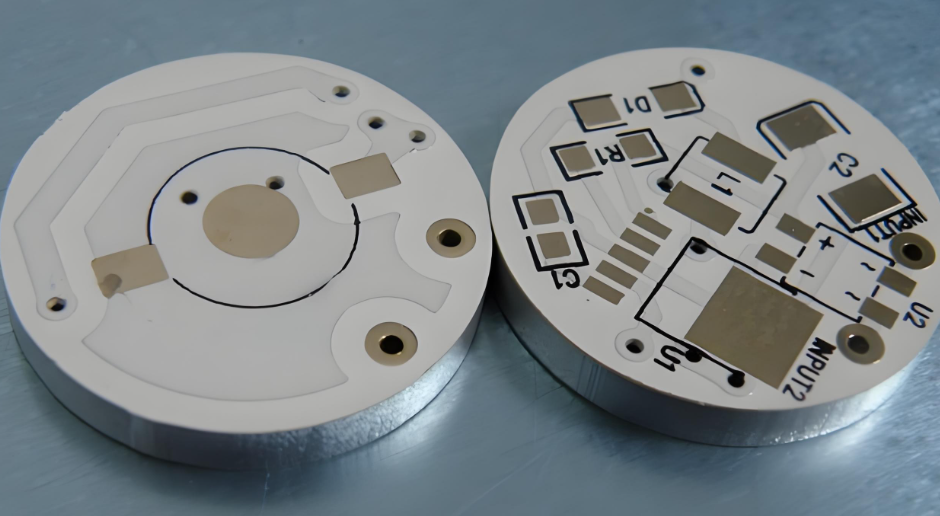
Metal core PCB material is selected when a circuit board needs stronger heat dissipation than a standard FR4 board can provide. Instead of using only fiberglass epoxy as the base, a metal core PCB uses aluminum, copper, or another metal substrate to transfer heat away from components such as LEDs, power ICs, MOSFETs, voltage regulators, motor drivers, and automotive lighting modules.

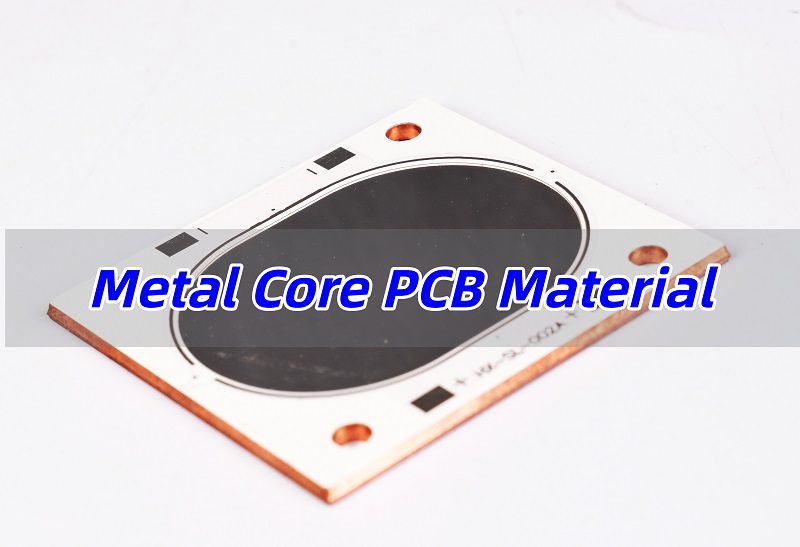
A typical metal core PCB has three key parts: the copper circuit layer, the thermally conductive dielectric layer, and the metal base. The copper layer carries electrical signals and current. The dielectric layer provides insulation while helping heat move downward. The metal base spreads that heat into the housing, heat sink, chassis, or surrounding air.

For many projects, aluminum is the most practical choice. For higher-power or high-current designs, copper may be a better fit. The final choice depends on heat load, current level, board size, insulation requirement, product environment, and cost target.
Metal Core PCB Material
Metal core PCB Material

What Is Metal Core PCB Material?

Metal core PCB material refers to the material system used to build a metal core printed circuit board. It is not only the metal base. It also includes the copper foil, insulation layer, solder mask, surface finish, and sometimes special thermal interface materials.

The main purpose of this material system is to move heat away from components more efficiently. In a standard FR4 PCB, heat moves slowly through the fiberglass epoxy base. In a metal core PCB, heat can travel through a thermal dielectric layer into a metal substrate, which spreads heat across a larger area.

A common metal core PCB stack-up includes:

LayerMain FunctionWhy It Matters
Solder maskProtects copper traces and prevents solder bridgingImproves surface protection and assembly reliability
Copper circuit layerCarries current and electrical signalsDefines circuit performance and current capacity
Thermal dielectric layerTransfers heat while providing electrical insulationA key factor in thermal resistance
Metal coreSpreads and conducts heatUsually aluminum or copper
Surface finishProtects exposed copper padsSupports solderability and assembly quality

Metal core PCBs are often called MCPCB, IMS PCB or insulated metal substrate PCB. They are widely used in LED lighting, automotive lighting, power electronics, motor control, industrial modules, and thermal management products.

What Materials Are Used in a Metal Core PCB?

The most common materials used in a metal core PCB are aluminum, copper, thermal dielectric material, copper foil, solder mask, and surface finish materials. Each one affects thermal performance, electrical safety, mechanical strength, and manufacturing cost.

Aluminum is the most widely used metal base because it offers a good balance between thermal performance, weight, machinability, and price. Copper provides stronger heat spreading and current-carrying capability, but it is heavier and more expensive. The dielectric layer is especially important because it must conduct heat and insulate electricity at the same time.

MaterialCommon RoleTypical ApplicationSelection Note
Aluminum coreMain heat-spreading baseLED lighting, power supply, automotive lightingBest balance for cost and thermal performance
Copper coreHigh-performance heat-spreading baseHigh-power modules, RF, high-current electronicsBetter thermal conduction but higher cost
Thermal dielectricHeat transfer and electrical insulationAll metal core PCB structuresA major factor in thermal resistance
Copper foilElectrical circuit layerSignal and power traces1oz, 2oz, 3oz or heavier copper may be used
Solder maskSurface protectionMost assembled PCBsMust withstand assembly and operating conditions
ENIG / HASL / OSPSurface finishSolder pads and exposed copper areasChosen based on assembly, shelf life, and cost

Public manufacturing specifications often show dielectric thermal conductivity options around 1W/m·K, 2W/m·K, 3W/m·K, or higher, while metal thickness may range from about 0.4mm to 3.2mm depending on supplier capability and design class.

Why Is Aluminum the Most Common Metal Core PCB Material?

Aluminum is the most common metal core PCB material because it gives designers a practical mix of heat dissipation, light weight, stable mechanical support, and manufacturability. It is widely used when the product needs better thermal control than FR4 but does not require the cost level of copper core PCB.

Aluminum core PCB is especially common in LED products. LED chips are sensitive to temperature, and poor heat transfer can reduce luminous efficiency and shorten service life. An aluminum substrate helps move heat from the LED package into the board and then into the fixture body or heat sink.

Aluminum core PCB is also common in:

  • LED bulbs and LED modules
  • Automotive headlights and taillights
  • Street lighting and high-bay lighting
  • Power supply boards
  • Motor control electronics
  • Battery charging products
  • Industrial control modules
  • Consumer power devices

Aluminum PCBs are commonly available in thicknesses such as 1.0mm, 1.5mm, 1.6mm, and 2.0mm, with copper thickness often selected from 1oz to 3oz for many thermal and power designs. Public capability tables from PCB manufacturers show aluminum PCB thickness ranges from about 0.3mm to 3.0mm, with special options available for thicker structures.

Aluminum is not always the highest-performance choice, but it is often the best commercial choice. When the heat load is moderate and the project needs stable quality at a reasonable cost, aluminum core PCB is usually the first material to evaluate.

When Should You Choose Copper Core PCB Material?

Copper core PCB material should be considered when the design has high heat density, high current, compact board size, or strict reliability requirements. Copper spreads heat faster than aluminum and can support demanding thermal paths in power electronics, RF modules, automotive systems, and aerospace-grade assemblies.

Copper core PCB is suitable for applications such as:

  • High-power LED modules
  • Power converters and inverters
  • High-current control boards
  • RF and microwave power modules
  • Automotive power electronics
  • Aerospace electronics
  • Laser diode modules
  • High-reliability industrial equipment

The main value of copper core material is its stronger thermal conductivity and current-handling potential. When heat is concentrated in a small area, copper can spread it more quickly across the board. This helps reduce hot spots and improve thermal stability.

However, copper core PCB also requires more careful cost control. Copper is heavier and more expensive than aluminum. It can also be more challenging to machine, drill, and process. For this reason, copper core material is usually selected when the design clearly needs the extra thermal performance.

A good approach is to start with the thermal requirement, not the material name. If aluminum with a high-performance dielectric layer can meet the junction temperature target, it may be the more economical solution. If the design still has heat concentration or current stress, copper core becomes a stronger option.

Is Copper Core Better Than Aluminum Core?

Copper core is better than aluminum core for maximum thermal spreading and high-current applications, but aluminum core is better for many cost-sensitive and weight-sensitive products. The better choice depends on heat load, budget, board size, mechanical structure, and reliability target.

Comparison ItemAluminum Core PCBCopper Core PCB
Thermal performanceGoodExcellent
WeightLighterHeavier
CostLowerHigher
Machining difficultyEasierMore difficult
Current supportGood for many power designsBetter for high-current structures
Common useLED lighting, power supply, automotive lightingHigh-power electronics, RF, aerospace, heavy-current modules
Best fitBalanced thermal and cost requirementsHigh heat density or high reliability requirements

For most LED lighting and general power products, aluminum core PCB is enough. For high-power density modules, copper core PCB can be a better investment because it improves heat spreading and reduces thermal stress.

A practical selection rule is simple:

Choose aluminum core when the design needs reliable heat dissipation at a controlled cost. Choose copper core when the product has concentrated heat, high current, limited cooling space, or strict thermal margins.

How Important Is the Dielectric Layer in Metal Core PCB Material?

The dielectric layer is one of the most important parts of metal core PCB material. It sits between the copper circuit and the metal base. Its job is difficult because it must conduct heat while preventing electrical current from reaching the metal core.

Many buyers focus only on whether the board is aluminum or copper. In real thermal design, the dielectric layer can be the bottleneck. Even when the metal base has strong thermal conductivity, heat still needs to pass through the dielectric first.

Important dielectric layer parameters include:

ParameterWhy It Matters
Thermal conductivityHigher values help heat move through the insulation layer
Dielectric thicknessThinner layers often reduce thermal resistance
Breakdown voltageEnsures electrical insulation safety
Peel strengthHelps copper stay bonded to the dielectric
Glass transition and thermal stabilitySupports soldering and long-term operation
Moisture resistanceHelps reliability in humid or outdoor applications

Typical metal core PCB dielectric materials may offer thermal conductivity from about 1W/m·K to 4W/m·K, with higher grades available from some material systems. Conventional MCPCB structures often rely on the dielectric layer as the main thermal path between copper traces and the metal base.

For LED and power electronics, the dielectric layer should be selected together with component power loss, copper area, board thickness, housing structure, and expected operating temperature. A high-conductivity dielectric may cost more, but it can improve product stability when the heat source is intense.

What Thickness Is Best for Metal Core PCB Material?

The best metal core pcb thickness depends on heat dissipation, mechanical strength, current level, product structure, and assembly requirements. There is no universal thickness that fits every project. Many metal core PCBs use total board thicknesses around 1.0mm, 1.5mm, 1.6mm, or 2.0mm, while special designs may use thinner or thicker structures.

Thickness selection should consider three areas: total board thickness, metal base thickness, and dielectric thickness.

Thickness ItemCommon RangeSelection Guidance
Total board thickness0.8–3.0mm commonChoose based on mechanical support, fixture design, and heat path
Aluminum base thickness0.5–2.0mm commonThicker base improves rigidity and heat spreading
Copper foil thickness1oz–3oz commonHigher current often needs thicker copper
Dielectric thickness75–150μm common; some specs show wider rangesThinner dielectric can improve heat transfer but must meet voltage needs
Metal thickness capabilityAround 0.4–3.2mm in some public specificationsDepends on manufacturer capability and stack-up

Some public MCPCB manufacturing data lists metal thickness around 0.4–3.2mm and dielectric thickness around 100–300μm, depending on standard or advanced capability.

For LED boards, 1.5mm or 1.6mm aluminum core PCB is commonly selected because it offers good mechanical stability and familiar assembly handling. For automotive lighting or higher-power designs, thicker metal bases may be used to increase heat spreading and structural strength.

When selecting thickness, avoid looking at only the total board number. A 1.6mm metal core PCB can behave very differently depending on copper thickness, dielectric thickness, dielectric thermal conductivity, and base metal type.

Metal Core PCB vs FR4: Which Is Better for Heat Dissipation?

Metal core pcb vs fr4 is mainly a heat dissipation comparison. Metal core PCB is better for heat dissipation because its aluminum or copper substrate spreads heat faster than fiberglass epoxy. FR4 is still suitable for general electronic products, signal circuits, control boards, and multilayer routing, but it is not the first choice for high-power thermal designs.

FR4 is widely used because it is cost-effective, easy to process, and suitable for multilayer circuits. However, when components generate significant heat, FR4 often needs extra thermal vias, copper pours, heat sinks, or larger board area. Metal core PCB creates a more direct heat path from the component to the metal base.

FeatureFR4 PCBMetal Core PCB
Base materialFiberglass epoxy laminateAluminum, copper, or metal alloy
Thermal performanceLimitedStrong
Typical thermal conductivityAround 0.3W/m·K for many FR4 materialsOften much higher through thermal dielectric systems
Best useGeneral electronics, control circuits, multilayer designsLEDs, power modules, thermal products
Layer complexityVery flexible for multilayer routingMore limited, especially in simple MCPCB structures
Mechanical rigidityGoodVery strong
CostUsually lowerUsually higher
Heat sink integrationOften needs extra design workEasier to connect to housing or heat sink

FR4 thermal conductivity is often cited around 0.25–0.3W/m·K, while MCPCB dielectric systems are commonly listed around 1–4W/m·K or higher depending on material grade.

Choose FR4 when the circuit is low-power, routing density is high, or cost control is the main goal. Choose metal core PCB when heat is a primary design concern, especially for LEDs, power devices, automotive lighting, and compact electronics with limited cooling space.

How to Choose the Right Metal Core PCB Material for Your Design?

To choose the right metal core PCB material, start with the heat source and working environment. Then match the metal base, dielectric layer, copper thickness, surface finish, and board thickness to the actual product requirement.

A clear selection process helps reduce redesign risk:

1. Identify the heat source

List the components that generate heat, such as LEDs, MOSFETs, power ICs, regulators, bridge rectifiers, or high-current connectors.

2. Estimate power loss

Check how much heat the component will generate during normal and peak operation. Use this to define the thermal path.

3. Choose aluminum or copper core

Use aluminum for most balanced thermal designs. Use copper when heat density or current level is high.

4. Select dielectric thermal conductivity

For general LED and power designs, 1–2W/m·K may be enough. For compact or high-power designs, 3W/m·K or higher may be considered.

5. Check dielectric thickness and voltage requirement

A thinner dielectric can improve heat transfer, but it must still meet insulation and breakdown voltage requirements.

6. Define copper thickness

For low-to-medium current circuits, 1oz copper may be enough. For power boards, 2oz or 3oz copper is often considered.

7. Confirm total metal core pcb thickness

Match the board thickness with mechanical mounting, housing flatness, screw holes, thermal interface material, and assembly process.

8. Review surface finish

ENIG, HASL, lead-free HASL, and OSP may be selected depending on assembly, shelf life, solderability, and cost.

9. Discuss DFM before production

Before mass production, the stack-up, hole design, outline tolerance, solder mask clearance, copper spacing, thermal pad design, and assembly method should be reviewed.

A strong MCPCB design is not built by choosing the most expensive material. It is built by matching the right material to the real thermal path.

Why Choose EBest Circuit as Your Metal Core PCB Manufacturer?

Choosing the right metal core pcb manufacturer is important because MCPCB quality depends on material selection, lamination control, dielectric reliability, copper bonding, surface finish, machining accuracy, and thermal performance. A small stack-up mistake can affect heat transfer, soldering, assembly, and long-term stability.

EBest Circuit supports metal core PCB projects from early design review to fabrication, assembly, and testing. For customers developing LED lighting, automotive electronics, industrial controls, power modules, medical electronics, communication products, and UAV systems, EBest can help review the material stack-up before production.

EBest Circuit can support:

  • Aluminum core PCB manufacturing
  • Copper core PCB manufacturing
  • DFM review before fabrication
  • Thermal material and stack-up suggestions
  • Prototype and small-batch production
  • PCB fabrication and PCBA assembly
  • Component sourcing and BOM support
  • AOI, X-ray, electrical testing, and process inspection
  • Quality control for regulated and high-reliability applications

For customers who are not sure whether to use aluminum core, copper core, or FR4, EBest can review the drawing, Gerber file, BOM, current load, heat source, and application environment. This helps avoid over-design and under-design.

A reliable metal core PCB manufacturer should not only produce the board. It should help customers make practical decisions about thermal conductivity, dielectric thickness, copper weight, surface finish, and assembly risk.

FAQs

1. What is metal core PCB material?

Metal core PCB material is the material system used in a metal core printed circuit board. It usually includes a copper circuit layer, thermal dielectric layer, and aluminum or copper metal base. Its main purpose is to improve heat dissipation.

2. What is the most common metal core PCB material?

Aluminum is the most common metal core PCB material. It offers a good balance of thermal performance, weight, cost, and manufacturability, making it suitable for LED lighting, power supplies, automotive lighting, and industrial electronics.

3. Is copper core better than aluminum core?

Copper core is better for high thermal conductivity and high-current designs. Aluminum core is better for many projects that need reliable heat dissipation at a more controlled cost. The better choice depends on heat load, budget, and application.

4. What is the normal metal core pcb thickness?

Common metal core pcb thickness options include 1.0mm, 1.5mm, 1.6mm, and 2.0mm. Some projects may use thinner or thicker boards depending on heat dissipation, mechanical structure, and assembly requirements.

5. Is metal core PCB better than FR4?

Metal core PCB is better than FR4 for heat dissipation. FR4 is better for general electronics, complex multilayer routing, and cost-sensitive low-power circuits. For LEDs, power modules, and automotive lighting, metal core PCB is often the better thermal choice.

6. What is the dielectric layer in metal core PCB material?

The dielectric layer is the insulating layer between the copper circuit and the metal base. It transfers heat while preventing electrical current from reaching the metal core. Its thermal conductivity and thickness strongly affect board performance.

7. Can metal core PCB be multilayer?

Yes, metal core PCB can be designed as single-layer, double-layer, or more complex structures. However, multilayer MCPCB requires careful stack-up design, insulation control, drilling process, and manufacturer review.

8. How do I choose a metal core PCB manufacturer?

Choose a metal core PCB manufacturer with material knowledge, DFM support, stable fabrication capability, thermal stack-up experience, testing systems, and PCB assembly support. For high-power or high-reliability products, early engineering review is especially valuable.

Conclusion

Need support with metal core PCB material selection or MCPCB manufacturing? Contact EBest Circuit for DFM review, material suggestions, PCB fabrication, PCBA assembly, and prototype-to-production support.
You may also like

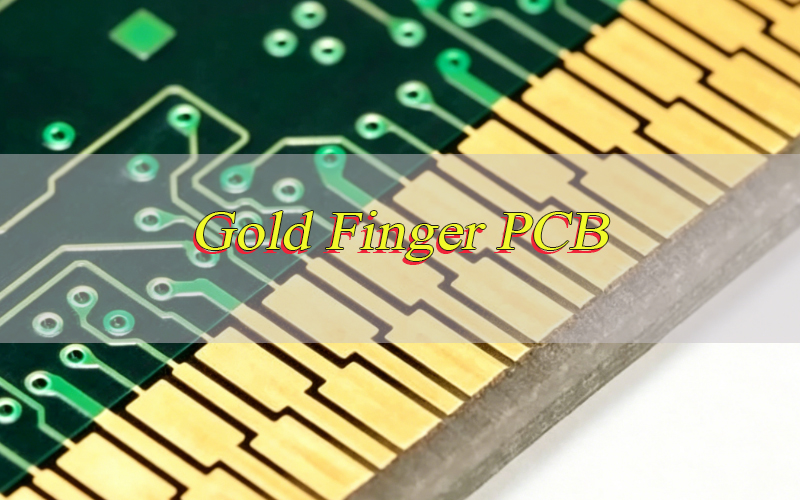
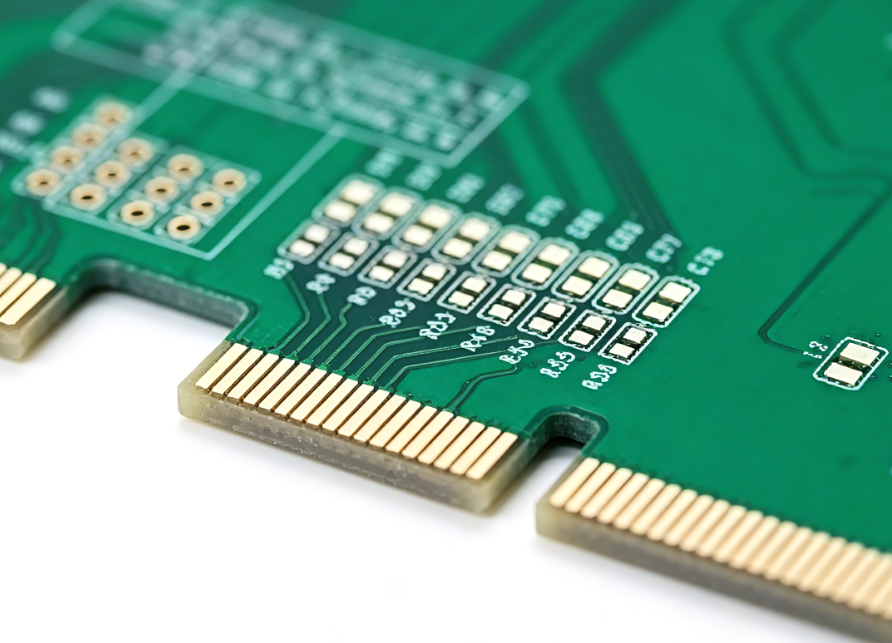
Gold Finger PCB Bevel & Plating Process: Design Tips and Reliable Manufacturer Guide

May 11th, 2026

Which factors most directly impact the performance, durability, and signal stability of gold finger PCB, and how can design and manufacturing missteps that lead to product failure be avoided? This guide breaks down standard bevel angles, plating processes, thickness selection, design principles, and manufacturer identification to provide practical, actionable insights for gold finger PCB that meets application demands and maintains long-term reliability.

Gold Finger PCB

What Is the Standard PCB Gold Finger Bevel Angle and How to Design It Properly?

PCB gold finger typically uses a standard bevel angle between 30 and 45 degrees, with 45 degrees being the most widely adopted for most use cases. This range balances mechanical protection, smooth insertion, and effective contact area to prevent damage to the gold plating during insertion while ensuring consistent electrical connectivity. Stepping outside this range often leads to performance issues.

  • Standard Angle Ranges and Application Scenarios: A 45-degree angle works best for vertical insertion setups such as memory modules and graphics cards, as it provides smooth guidance to minimize friction and scratching of the gold layer during insertion. A 30-degree angle is better suited for horizontal insertion applications like PCIe slots, as it reduces contact pressure and lessens wear on both the gold finger and its mating connector. Angles below 20 degrees create sharp edges that scratch mating contacts and cause uneven plating due to current concentration. Angles above 60 degrees reduce the effective contact area and drive up contact resistance.
  • Design Considerations for Bevel Angles: Start by matching the angle to the insertion method. Vertical insertion calls for a steeper 45-degree angle for guidance, while horizontal insertion requires a shallower 30-degree angle to reduce pressure. Bevel depth should fall between 0.5mm and 1.0mm. Depths under 0.5mm fail to provide adequate guidance, and depths over 1.0mm weaken the PCB’s edge structure. Maintain a minimum 0.5mm gap between the bevel edge and the nearest circuit trace to prevent trace damage during bevel processing.
  • Manufacturing Feasibility Checks: For electroless nickel gold plating processes, the bevel angle should not drop below 30 degrees. Electroless plating deposits more slowly on sharp edges, resulting in thin, inconsistent plating. Electroplating processes can handle angles as low as 20 degrees but require fixtures to control current distribution and avoid excessive edge plating. Clearly note the bevel angle, depth, and tolerance on design drawings. Angles should have a ±5-degree tolerance, and depth a ±0.15mm tolerance.

What Are the Steps in the PCB Gold Finger Plating Process?

The PCB gold finger plating process includes eight core steps. Strict control of each step’s parameters ensures uniform plating, strong adhesion, and corrosion resistance. The two most common processes, electroless nickel immersion gold (ENIG) and electrolytic gold plating, require slight adjustments to these steps based on the method used.

  • Pre-Plating Surface Preparation: Clean the PCB surface to remove oil, oxides, and contaminants. Begin with an organic acid-based degreaser to eliminate oil and reduce surface tension for even solution coverage. Rinse thoroughly with deionized water after degreasing. Next, microetch the copper surface using a sodium persulfate solution to remove thin oxide layers and create a slightly rough surface that improves nickel layer adhesion. Keep copper ion concentration in the microetch solution between 3-20g/L to maintain a stable etching rate.
  • Acid Pickling and Pre-Dipping: Use dilute sulfuric acid to remove oxides formed after microetching and any residual salts. Rinse with deionized water, then immerse the PCB in a pre-dip solution (AR grade sulfuric acid) to maintain the activation tank’s acidity and keep the copper surface fresh for effective activation in the next step.
  • Activation Treatment: Immerse the PCB in a palladium activation solution to form a thin palladium layer on the copper surface via displacement reaction. This palladium layer acts as a catalyst for the subsequent electroless nickel plating. Keep activation temperature below 30℃, avoid aeration, and ensure the solution is free of chloride, iron, or nickel impurities to prevent activation failure.
  • Electroless Nickel Plating: Deposit a nickel layer on the activated copper surface. This layer acts as a barrier between copper and gold to prevent mutual diffusion. Control plating temperature between 80-90℃ and pH between 4.5-5.5. The nickel layer should be 2-5μm thick for sufficient adhesion and corrosion resistance, with a uniform finish free of pinholes or bubbles.
  • Gold Plating: For ENIG processes, immerse the PCB in an immersion gold solution to replace nickel with gold, forming a thin (0.1-0.3μm) yet highly conductive gold layer. For electrolytic gold plating, use an electrolytic solution with gold cyanide as the main component and apply a constant current to deposit a thicker (1-5μm) gold layer ideal for high-wear applications. Maintain gold purity above 99.9% for optimal electrical performance.
  • Gold Recovery and Rinsing: Recover excess gold from the gold plating solution to reduce costs and environmental impact. Rinse the PCB thoroughly with deionized water multiple times to remove residual plating chemicals that can cause corrosion if left on the surface.
  • Post-Plating Cleaning and Drying: Clean the PCB surface with a dilute sulfuric acid or citric acid solution to remove any remaining impurities, then dry it in a high-temperature oven (80-100℃) to prevent moisture-induced oxidation of the gold layer.
  • Quality Inspection: Use a thickness gauge to verify nickel and gold layer thickness. Check for plating defects like unevenness, copper exposure, bubbles, or scratches. Conduct adhesion tests (tape tests) to ensure the plating layer does not peel when tape is applied and removed.
gold finger PCB

How to Choose the Right PCB Gold Finger Plating Thickness for Different Projects?

Selecting the correct PCB gold finger plating thickness depends on three core factors: insertion frequency, application environment, and electrical performance requirements. Thicker gold layers boost wear resistance but increase costs, while thinner layers reduce costs but may not meet durability needs. Aligning thickness with project requirements ensures optimal performance and cost-effectiveness.

  • Consumer Electronics Applications: For devices with low insertion frequency (fewer than 1,000 cycles) such as USB dongles, mobile phone chargers, and tablet connectors, a thin gold layer (0.1-0.3μm) using ENIG is sufficient. This thickness balances cost and basic corrosion resistance. For devices with moderate insertion frequency (1,000-5,000 cycles) like memory modules and external hard drives, a 0.5-1.0μm gold layer ensures durability.
  • Industrial Control Applications: Industrial equipment including PLC controllers, sensors, and server motherboards requires high durability (5,000-10,000 insertion cycles) and resistance to harsh environments. A 1.0-3.0μm gold layer using electrolytic gold plating is ideal. The nickel layer should be 3-5μm thick to enhance corrosion resistance in high-humidity and dusty settings.
  • Aerospace and Military Applications: These applications demand extreme durability (10,000+ insertion cycles) and resistance to extreme temperatures, vibration, and corrosion. A 3.0-5.0μm gold layer with high purity (99.99%) is required. The nickel layer should be 5-8μm thick, and additional corrosion protection such as conformal coating may be necessary.
  • High-Speed Signal Applications: For high-speed devices like 5G base stations and PCIe 5.0 interfaces, a thin (0.1-0.2μm) high-purity gold layer is preferred. Thicker gold layers can increase signal loss and impedance mismatch. ENIG ensures a smooth surface that reduces signal reflection and insertion loss.
  • Key Considerations: Gold layer thickness is not a case of “thicker is better.” Thickness exceeding 5μm can create internal stress in the gold layer, leading to cracking or peeling. Match gold thickness to nickel layer thickness; the nickel layer should be 3-5 times the gold layer thickness to ensure strong adhesion. Electrolytic gold plating is more expensive than ENIG, so use it only when high wear resistance is necessary.

What Are the Critical Design Principles for High-Quality Gold Finger PCB?

Designing high-quality gold finger PCB requires balancing electrical performance, mechanical durability, and manufacturing feasibility. Following these critical principles avoids common design flaws such as poor contact, plating peeling, and signal interference to ensure the product meets application requirements.

  • Bevel and Edge Design: Stick to the standard 30-45 degree bevel angle range and 0.5-1.0mm depth. Round the gold finger’s corners to avoid sharp edges that scratch mating connectors and damage the plating. Ensure the gold finger extends 2mm beyond the mating connector’s contact area to guarantee full contact.
  • Solder Mask Design: Do not apply solder mask to the gold finger area. Keep the solder mask fully open to prevent ink peeling during insertion, which can cause contact failure. The solder mask opening should be 4mil larger than the gold finger line on each side, and no solder mask openings should be placed within 2mm of the gold finger.
  • Circuit Trace Design: Keep gold finger lead widths between 12-40mil, with main leads at 40mil and secondary leads at 20mil. Use rounded corners for leads to avoid right-angle bends that cause signal reflection. Maintain a minimum 6mil spacing between adjacent gold fingers to prevent short circuits and crosstalk.
  • Plating Layer Matching: Use a nickel barrier layer between the copper substrate and gold layer to prevent copper-gold diffusion, which degrades electrical performance. The nickel layer thickness should be 2-8μm depending on the application, and the gold layer thickness should align with insertion frequency and environment.
  • PCB Thickness and Material Selection: PCB thickness should be 0.8-2.4mm, matching the mating connector’s slot thickness. Use high-quality FR-4 substrate for general applications and polyimide substrate for high-temperature or flexible applications. Ensure the substrate has good dimensional stability to prevent warpage that can disrupt gold finger alignment.
  • Test Point Design: Add test points near the gold finger to facilitate electrical testing of contact resistance and signal integrity. Place test points 1-2mm away from the gold finger to avoid interfering with plating and insertion.
Gold Finger PCB

How to Ensure Signal Integrity in Gold Finger PCB Design for High-Speed Applications?

High-speed applications including 5G, PCIe 5.0, and high-frequency radar require gold finger PCB to maintain signal integrity by minimizing signal reflection, insertion loss, and crosstalk. Control impedance matching, reduce signal attenuation, and optimize layout design to achieve this.

  • Impedance Matching Design: The gold finger and its connected transmission lines should have consistent impedance, typically 50Ω or 75Ω depending on the application. Calculate the gold finger width (for example, 0.8mm for 50Ω impedance on FR-4 substrate) and length (no more than 8mm) to avoid impedance sudden changes. Use a microstrip line extension structure with a 1mm gradual transition to create a smooth connection between the gold finger and transmission line, reducing return loss.
  • Minimize Insertion Loss: Use high-purity gold (99.99%) for the gold layer to reduce conductor loss. Keep the gold layer thin (0.1-0.2μm) to avoid excessive signal absorption. Polish the gold finger surface to ensure a smooth finish (Ra ≤ 0.10μm) that reduces signal loss caused by surface roughness.
  • Reduce Crosstalk: Maintain a minimum 1mm spacing between adjacent gold fingers. Arrange high-speed signal gold fingers alternately with ground fingers to form a shielding structure that reduces electromagnetic interference. Use equal-length design for gold finger leads, with a length difference of no more than 0.1mm to avoid signal time delay.
  • Shielding and Grounding: Add a ground plane below the gold finger area to provide a reference ground and reduce signal radiation. Connect the ground plane to the gold finger’s ground leads with multiple vias to improve grounding effectiveness. Avoid placing high-speed signal traces near the gold finger edge to prevent signal leakage.
  • Material Selection: For high-speed applications, use low-loss substrate materials like FR-4 with a low dielectric constant (εr ≤ 4.5) and low loss tangent (tanδ ≤ 0.02). For ultra-high-speed signals (above 32Gbps), use advanced materials like PTFE to further reduce signal loss.

What Quality Standards Should Gold Finger PCB Meet for Industrial and Aerospace Use?

Gold finger PCB used in industrial and aerospace applications must meet strict quality standards to ensure reliability in harsh environments including extreme temperatures, vibration, humidity, and corrosion. These standards cover plating quality, mechanical performance, electrical performance, and environmental resistance.

  • Plating Quality Standards: Comply with IPC-4552, the industry standard for gold plating on PCB. Gold layer purity must be ≥99.9% for industrial use and ≥99.99% for aerospace use. Nickel layer thickness should be 3-8μm, and gold layer thickness 1.0-5.0μm depending on the application. Plating must be uniform, with no copper exposure, bubbles, scratches, or peeling. The tape test should show no plating detachment.
  • Mechanical Performance Standards: For industrial use, gold finger must withstand 5,000+ insertion cycles without significant wear or increased contact resistance. For aerospace use, this number rises to 10,000+ cycles. The PCB should have a flexural strength of ≥150MPa and no warpage exceeding 0.75mm per 100mm length. Bevel angles must meet a ±5-degree tolerance, and edge roughness should be Ra ≤ 0.10μm.
  • Electrical Performance Standards: Contact resistance must be ≤50mΩ and remain stable after 1,000 insertion cycles. Insulation resistance must be ≥10^10Ω at 500V DC. Dielectric strength should be ≥1kV/mm to prevent breakdown. For high-speed applications, insertion loss must be ≤0.3dB and crosstalk ≤-35dB.
  • Environmental Resistance Standards: Gold finger PCB must pass a 72-hour salt spray test (5% NaCl concentration) with no corrosion or plating peeling. It should withstand high-temperature testing (-55℃ to 125℃ for industrial use, -65℃ to 150℃ for aerospace use) without performance degradation. It must also pass a humidity test (85% relative humidity at 85℃ for 1000 hours) with no insulation failure.
  • Certification Requirements: Industrial gold finger PCB must meet ISO9001 and RoHS certification. Aerospace gold finger PCB must comply with AS9100 certification and meet MIL-STD-202 standards for environmental testing. All products must have full traceability of materials and manufacturing processes.

What Are the Common Challenges in Gold Finger PCB Manufacturing and How to Solve Them?

Gold finger PCB manufacturing involves complex processes. Common challenges include uneven plating, poor adhesion, plating peeling, copper exposure, and impedance mismatch. These issues can be resolved through strict process control, careful material selection, and thorough quality inspection.

  • Uneven Plating: This issue stems from uneven current distribution, impure plating solution, or inadequate surface preparation. Use fixtures to ensure uniform current distribution during electroplating. Regularly filter the plating solution to remove impurities. Strengthen pre-plating cleaning to ensure the copper surface is free of oil and oxides. Keep plating temperature and pH within the recommended range.
  • Poor Plating Adhesion: Insufficient microetching, contaminated activation solution, or improper nickel plating parameters cause poor adhesion. Extend microetching time slightly to create a rougher copper surface. Replace the activation solution regularly to avoid impurity contamination. Control nickel plating temperature and pH to ensure proper nickel layer formation. Conduct adhesion tests after plating to catch issues early.
  • Plating Peeling: Excessive internal stress in the gold layer, insufficient nickel layer thickness, or poor substrate quality lead to plating peeling. Limit gold layer thickness to less than 5μm to reduce internal stress. Ensure the nickel layer is 3-5 times the gold layer thickness. Use high-quality substrates with strong adhesion to the nickel layer. Avoid rapid temperature changes during drying that can build up stress.
  • Copper Exposure on Gold Finger: Incomplete solder mask opening, uneven plating, or scratches during handling cause copper exposure. Improve solder mask opening accuracy to ensure full coverage of the gold finger area. Increase plating time slightly to ensure complete coverage. Use anti-scratch packaging during handling and manufacturing. Carefully inspect the gold finger surface after plating.
  • Impedance Mismatch: Incorrect gold finger width, length, or substrate material leads to impedance mismatch. Calculate impedance accurately based on substrate parameters and adjust gold finger dimensions accordingly. Use low-loss substrate materials for high-speed applications. Test impedance after manufacturing and adjust the design if needed.

How to Identify a Reliable China Gold Finger PCB Manufacturer?

Choosing a reliable China gold finger PCB manufacturer is critical to ensuring product quality, on-time delivery, and responsive technical support. Evaluate certification, production capacity, quality control, technical capabilities, and customer service to make the right choice.
  • Certification and Compliance: The manufacturer should hold ISO9001 certification for quality management and RoHS certification for environmental compliance. For aerospace or military applications, verify AS9100 and MIL-STD-202 certifications. Ensure the manufacturer adheres to IPC standards for gold finger PCB manufacturing.
  • Production Capacity and Equipment: Confirm the manufacturer has advanced production equipment, including automatic vertical electroplating lines, thickness gauges, impedance testers, and AOI inspection equipment. Check that production capacity aligns with your order volume and delivery timeline. Automated production lines ensure consistent quality and reduce human error.
  • Quality Control System: A reliable manufacturer has a strict quality control system covering raw material inspection, in-process testing, and final inspection. Raw materials such as substrate and plating chemicals must undergo quality testing. In-process testing includes checks for plating thickness, adhesion, and impedance. Final inspection covers visual inspection, electrical testing, and environmental testing. Request quality control reports for previous orders.
  • Technical Capabilities: The manufacturer should have professional technical teams capable of providing design support, DFM analysis, and custom solutions. They should handle complex designs such as high-speed gold finger PCB and aerospace-grade products. Ask about their experience in your specific industry and request case studies or samples.
  • Customer Service and Delivery: Reliable manufacturers offer timely technical support and communication. They should respond to inquiries within 24 hours and provide clear order updates. Check their delivery record to ensure on-time delivery (a delivery rate of ≥98% is ideal). Ask about their after-sales service policy, including return and replacement options for defective products.
  • Pricing and Cost Transparency: The manufacturer should provide transparent pricing with no hidden fees. Compare quotes from multiple manufacturers, but avoid choosing the lowest price if it compromises quality. A reliable manufacturer will share a detailed cost breakdown and explain price differences based on materials and processes.
Gold Finger PCB

FAQs About Gold Finger PCB

Q1: Can damaged gold finger PCB be repaired, and what are the effective repair methods?

A1: Damaged gold finger PCB can be repaired based on damage severity: Minor oxidation: Clean with anhydrous alcohol/specialized cleaner and polish with an eraser. Moderate scratches/thin plating: Touch up with a professional gold plating pen (match original gold layer thickness). Severe copper exposure/deep scratches: Re-plate (strip old plating, reprocess surface, re-plate nickel and gold). Application note: Non-critical applications only; replace PCB for aerospace/high-reliability industrial use.

Q2: What factors should be considered when selecting a PCB gold finger connector?

A2: Select PCB gold finger connectors by matching these key factors: Connector slot thickness matches PCB thickness (0.8-2.4mm); gold finger extends 2mm beyond connector contact area; contact force 10-30g per pin; high-speed applications: low contact resistance (≤50mΩ) and low crosstalk; harsh environments: corrosion-resistant materials (stainless steel/nickel plating).

Q3: How to prevent gold finger PCB from oxidation during storage and use?

A3: Prevent gold finger oxidation with these measures: Store in sealed packaging with desiccants (relative humidity ≤60%); avoid direct hand contact (use gloves); harsh environments: apply conformal coating to non-contact areas; regular maintenance: clean with anhydrous alcohol to remove dust/contaminants.

Q4: What is the difference between hard gold and soft gold plating for gold finger PCB?

A4: Soft gold (99.99% pure): high conductivity/ductility, suitable for low-insertion-frequency applications. Hard gold (gold + 5-10% cobalt/nickel): higher hardness/wear resistance, ideal for high-insertion-frequency use. Selection principle: Choose based on insertion frequency and performance needs.

Q5: How to test the quality of gold finger PCB after manufacturing?

A5: Gold finger PCB quality testing methods: Use a thickness gauge to verify nickel/gold layer thickness; conduct tape test forplating adhesion; measure contact resistance (≤50mΩ) with a multimeter; test impedance for high-speed applications; conduct environmental tests (salt spray/high-temperature) for industrial/aerospace use; visually inspect for defects under a magnifying glass.

You may also like

1k Resistor Color Code: How to Identify a 1k Ohm Resistor?

May 8th, 2026

A 1k resistor color code is one of the first resistor markings many electronics beginners learn. It appears in LED circuits, Arduino projects, PCB prototypes, sensor modules, pull-up networks, pull-down networks, and many low-power electronic designs.

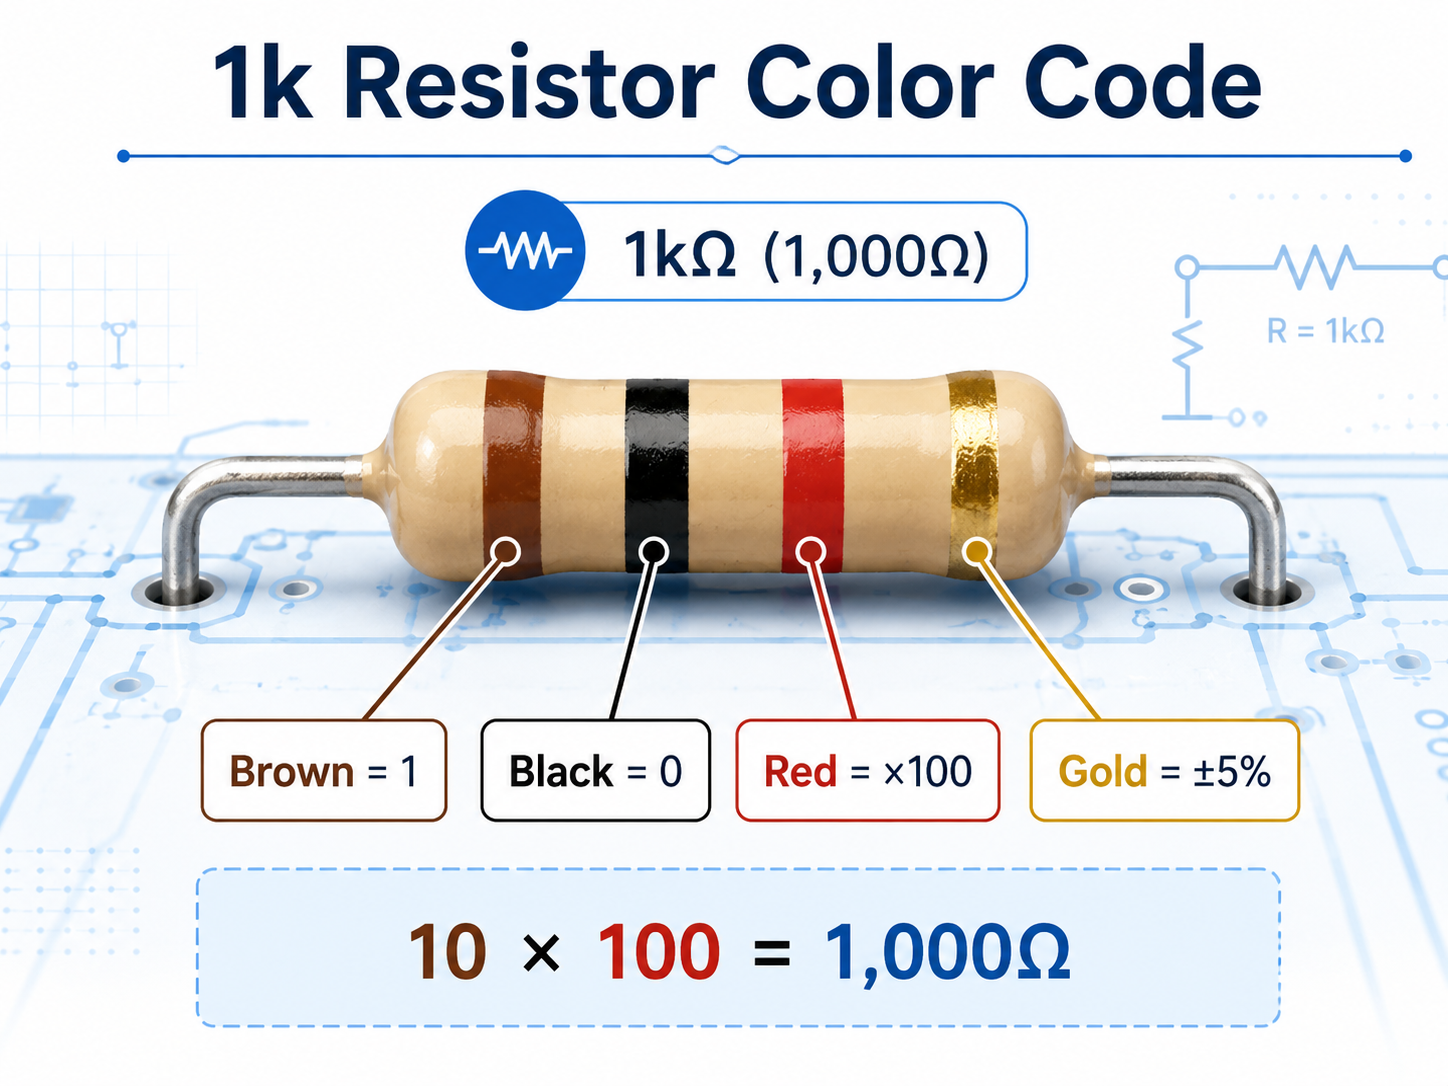
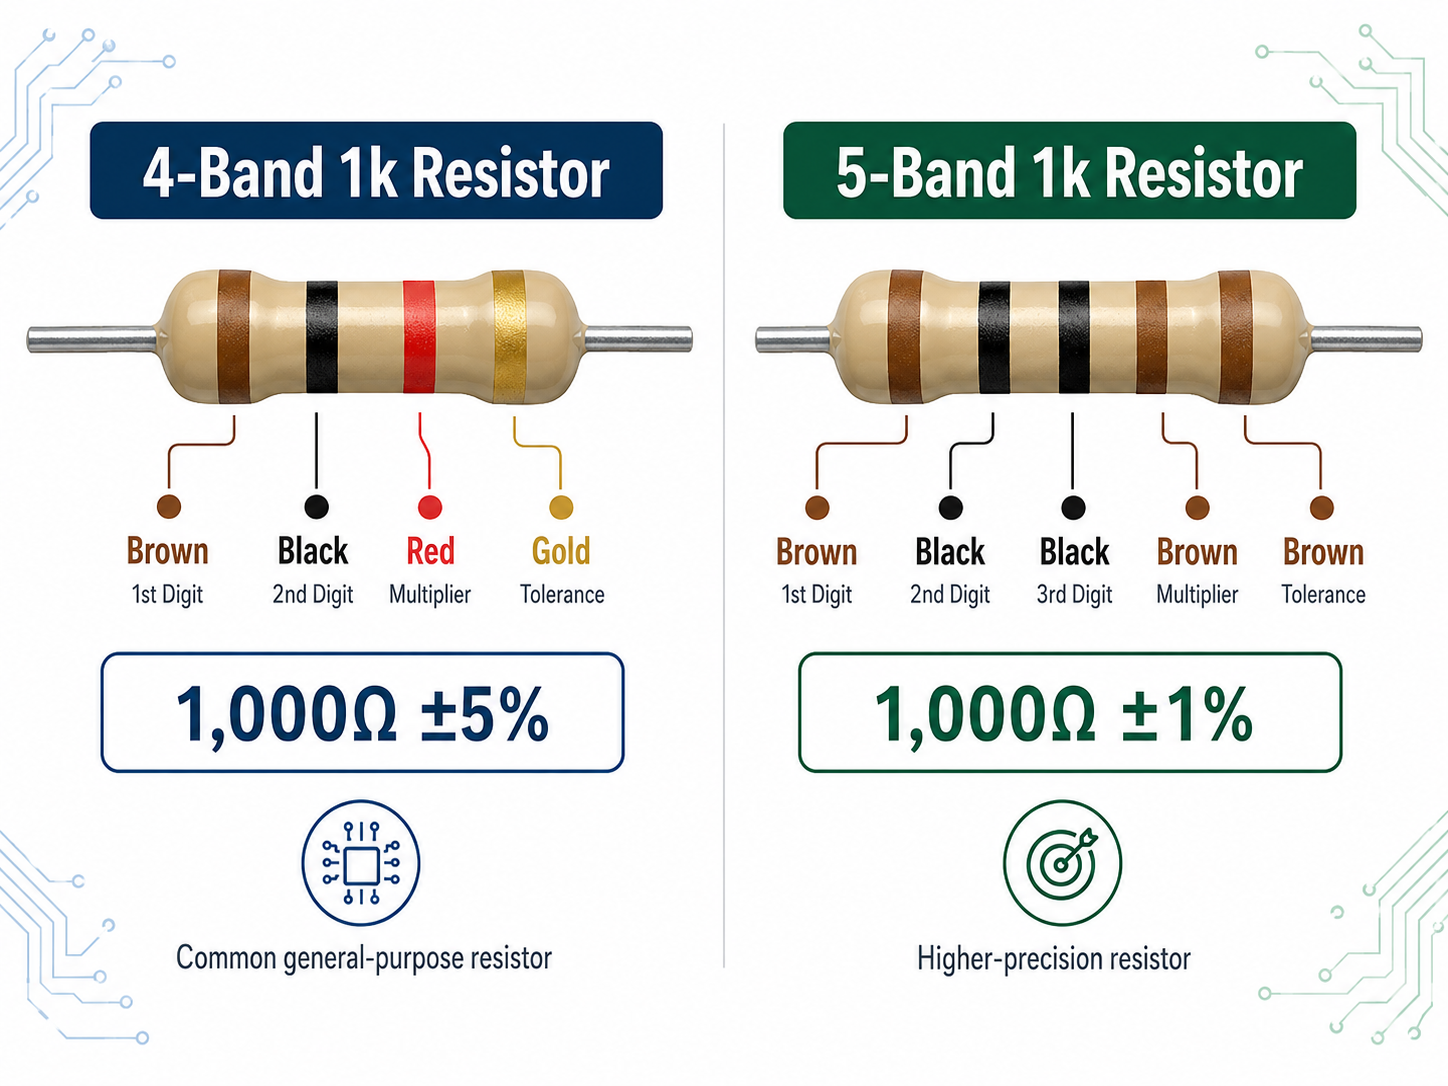
The value 1k means 1,000 ohms, also written as 1 kΩ. For a common 4-band resistor, the color code is:

Brown – Black – Red – Gold

For a 5-band precision resistor, the common color code is:

Brown – Black – Black – Brown – Brown

Both markings can represent a 1k ohm resistor, but the band count and tolerance are different. This guide explains how to read them clearly, how to identify a 1k resistor, how to test it, and how to understand its current and power limits.

1k Resistor Color Code: How to Identify a 1k Ohm Resistor?

What Is a 1k Resistor?

A 1k resistor is a passive electronic component with a resistance value of 1,000 ohms. Its job is to control current, divide voltage, set signal levels, protect components, and help circuits operate within safe electrical limits.

The letter k stands for kilo, which means one thousand. So when you see 1k resistor, it means:

1k resistor = 1,000 ohm resistor = 1 kΩ resistor

In real circuits, 1k resistors are extremely common because they offer a practical balance. They are large enough to limit current in many low-voltage circuits, yet small enough to allow useful signal flow.

You may find 1k resistors in:

  • LED current-limiting circuits
  • Microcontroller input and output circuits
  • Pull-up and pull-down resistor networks
  • Transistor base resistor designs
  • Sensor interface circuits
  • Audio and signal conditioning circuits
  • PCB test circuits
  • Prototype breadboard projects

In PCB assembly, 1k resistors are also widely used in surface-mount form. Instead of color bands, SMD resistors usually use printed numbers such as 102.

What Is a 1k Resistor Equal To?

A 1k resistor is equal to 1,000 ohms. It can also be written in several common ways depending on the circuit diagram, datasheet, BOM, or PCB silkscreen style.

MarkingMeaning
1k1,000 ohms
1 kΩ1,000 ohms
1000 Ω1,000 ohms
1.0k1,000 ohms
1K1,000 ohms
102 on SMD resistor1,000 ohms
0.001 MΩ1,000 ohms

In schematics, engineers often write 1k because it is shorter and easy to read. In datasheets and formal electrical documents, you may see 1 kΩ.

For SMD resistors, the code 102 is very common. The first two digits are 10, and the third digit tells how many zeros to add. So:

102 = 10 + two zeros = 1000 ohms

That means an SMD resistor marked 102 is usually a 1k ohm resistor.

What Color Is a 1k Resistor?

A standard 4-band 1k resistor usually has these colors:

Brown – Black – Red – Gold

Each color has a meaning:

BandColorMeaning
1st bandBrownFirst digit: 1
2nd bandBlackSecond digit: 0
3rd bandRedMultiplier: ×100
4th bandGoldTolerance: ±5%

So the value is:

10 × 100 = 1,000 ohms

The gold band means the resistor has a tolerance of ±5%. So a 1k resistor with gold tolerance can normally measure between:

950 ohms and 1,050 ohms

That is still considered acceptable for a ±5% resistor.

The body color of the resistor may vary. Many through-hole resistors have beige, tan, blue, green, or light-colored bodies. The body color itself is not the value. The colored bands provide the resistance information.

What Is the Color Code for a 1k Ohm Resistor?

The standard resistor color code for 1k ohm depends on whether the resistor uses 4 bands or 5 bands.

For a common 4-band resistor, the color code is:

Brown – Black – Red – Gold

This is the most familiar version for general electronics work.

ColorNumber or Function
Brown1
Black0
Red×100
Gold±5% tolerance

Calculation:

1, 0, ×100 = 1,000 ohms

So the color code for 1k ohm resistor in 4-band format is:

Brown Black Red Gold

Some 1k resistors may use a different tolerance color. For example:

4-Band Color CodeValueTolerance
Brown Black Red Gold1kΩ±5%
Brown Black Red Brown1kΩ±1%
Brown Black Red Red1kΩ±2%
Brown Black Red Silver1kΩ±10%

The first three bands still represent 1,000 ohms. The last band only changes the tolerance.

1k Resistor Color Code 5 Band

A 1k resistor color code 5 band version is usually used for precision resistors. A typical 5-band 1k resistor is:

Brown – Black – Black – Brown – Brown

Here is how it works:

BandColorMeaning
1st bandBrownFirst digit: 1
2nd bandBlackSecond digit: 0
3rd bandBlackThird digit: 0
4th bandBrownMultiplier: ×10
5th bandBrownTolerance: ±1%

Calculation:

100 × 10 = 1,000 ohms

So the value is again 1kΩ.

A 5-band resistor often provides better accuracy than a common 4-band resistor. For example, a 5-band 1k resistor with brown tolerance has a tolerance of ±1%. That means the acceptable measured range is usually:

990 ohms to 1,010 ohms

1k Resistor Color Code 5 Band

This tighter range is useful in circuits that need better precision, such as:

  • Measurement circuits
  • Voltage dividers
  • Sensor conditioning circuits
  • Analog signal circuits
  • Calibration networks
  • Industrial control electronics
  • Medical electronics circuits
  • Communication equipment

Not every 5-band resistor is automatically ±1%, but many precision resistors use the fifth band to show tighter tolerance.

What Does a 1000 Ohm Resistor Look Like?

A 1000 ohm resistor can look different depending on its package type.

For a traditional through-hole resistor, it is usually a small cylindrical component with two metal leads. It has several colored bands around the body. A common 1k through-hole resistor has the colors:

Brown – Black – Red – Gold

The resistor body may be beige, blue, green, or another coating color. The value is not determined by the body color. It is determined by the bands.

For an SMD resistor, the appearance is different. It is a small rectangular part mounted directly on the PCB surface. Instead of colored rings, it often has a number printed on top.

A 1k SMD resistor may be marked as:

SMD CodeMeaning
1021,000 ohms
10011,000 ohms in 4-digit code
1K01,000 ohms
01CEIA-96 code, may indicate 1k depending on tolerance series

The code 102 is the most common marking for a 1k SMD resistor in many general-purpose circuits.

In PCB assembly, SMD resistors are more common than through-hole resistors because they support automated SMT production, compact layouts, and high-density circuit design.

How to Identify a 1k Resistor?

You can identify a 1k resistor in several practical ways. The best method depends on whether the resistor is through-hole or surface-mount.

1. Check the color bands

For a 4-band resistor, look for:

Brown – Black – Red – Gold

For a 5-band resistor, look for:

Brown – Black – Black – Brown – Brown

Always read from the end where the tolerance band is farther away or separated slightly from the other bands. The tolerance band is often gold, silver, brown, or red.

2. Read the SMD code

For surface-mount resistors, check the printed marking. A 1k SMD resistor is commonly marked:

102

This means 10 followed by two zeros, giving 1000 ohms.

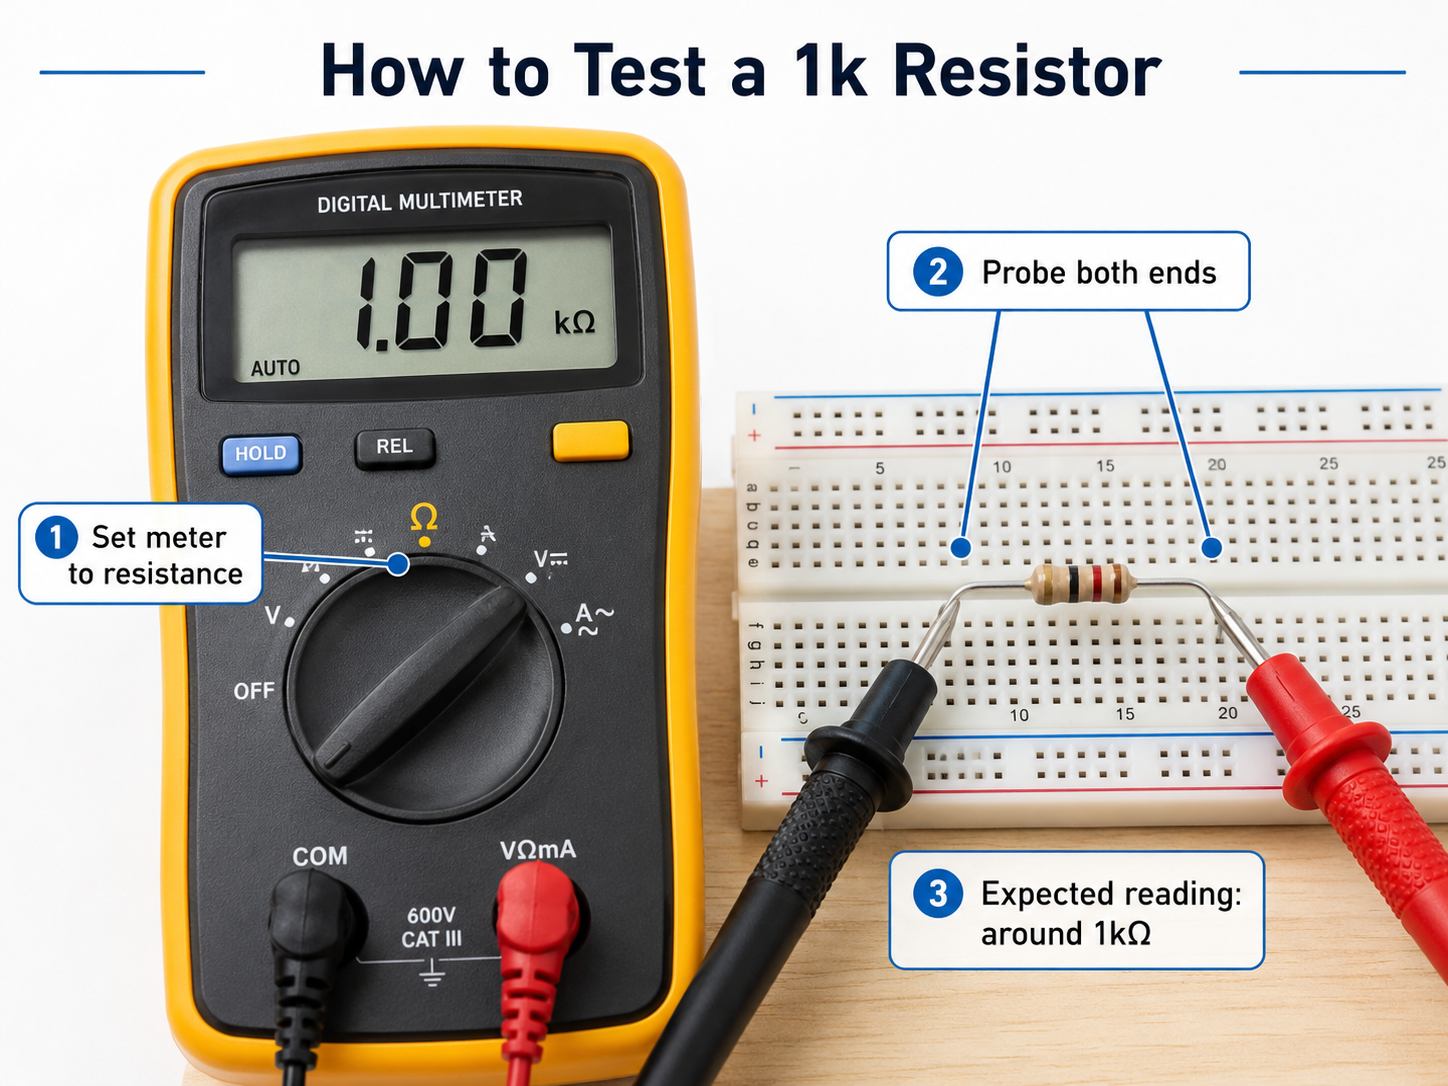
3. Use a multimeter

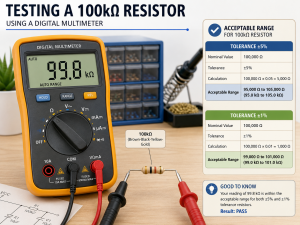
Set your multimeter to resistance mode. Touch one probe to each end of the resistor. A good 1k resistor should measure close to 1,000 ohms.

A ±5% resistor may show a value around 950–1050 ohms. A ±1% resistor may show around 990–1010 ohms.

4. Check the circuit schematic or BOM

In a PCB project, the resistor value is usually listed in the schematic, BOM, or assembly drawing. It may appear as:

  • R1 = 1k
  • R15 = 1 kΩ
  • 1K, 5%, 0603
  • 1kΩ, ±1%, 0805
  • 1000R

5. Look at the PCB designator

PCB silkscreen often marks resistors as R1, R2, R3, and so on. The silkscreen does not usually show the value, but it helps you match the component to the BOM.

What Are the Different Types of 1k Resistors?

A 1k resistor can come in many forms. The value is the same, but package, material, accuracy, power rating, and mounting style may be different.

TypeDescriptionCommon Use
Carbon film 1k resistorEconomical through-hole resistorBasic circuits, hobby projects
Metal film 1k resistorBetter tolerance and lower noiseAudio, analog, measurement circuits
Thick film SMD 1k resistorCommon surface-mount resistorGeneral PCB assembly
Thin film SMD 1k resistorHigher precision and stabilityPrecision electronics
Wirewound 1k resistorHigher power capabilityPower circuits, industrial equipment
Fusible 1k resistorDesigned to open safely under overloadProtection circuits
High-voltage 1k resistorBuilt for higher voltage stressPower supply circuits
Resistor networkMultiple resistors in one packagePull-up arrays, compact PCB layouts

For modern PCB assembly, SMD thick film resistors are widely used because they are cost-effective, compact, and suitable for automated placement.

Common SMD package sizes include:

PackageApproximate SizeTypical Use
0402Very smallCompact electronics
0603Small and commonConsumer and industrial PCBs
0805Easy to handlePrototypes, general PCBs
1206Larger sizeHigher power or easier assembly
1210 and aboveLarger footprintHigher power designs

The resistor package affects power rating and heat handling. A 1k resistor in 0402 size cannot handle the same power as a 1k resistor in 1206 size.

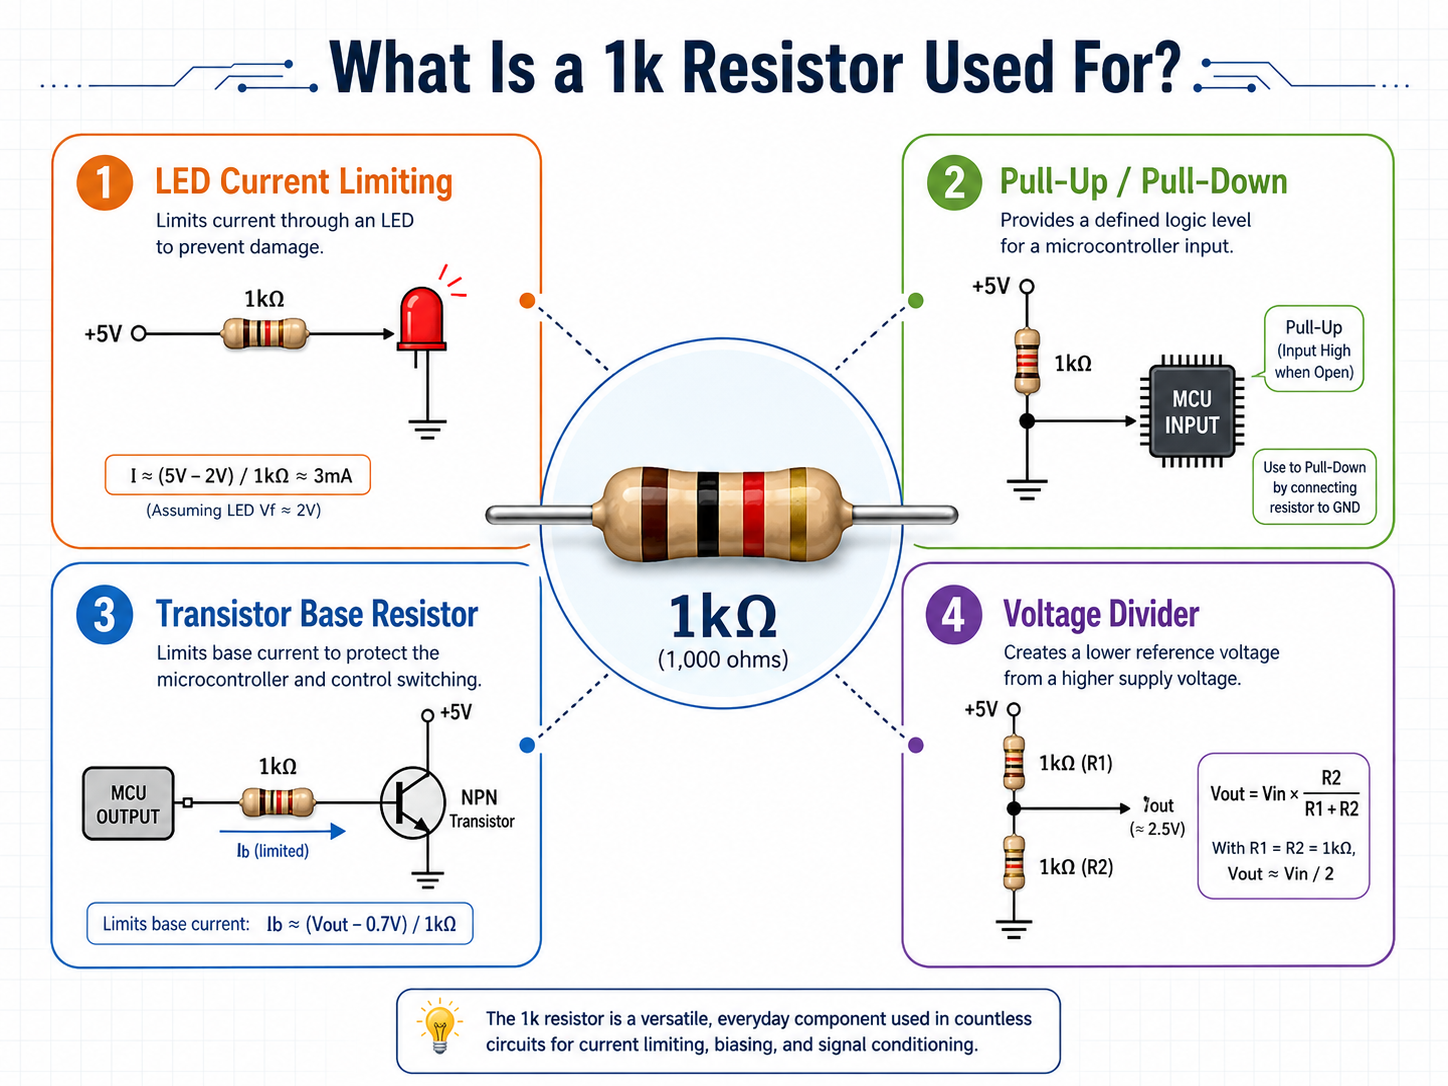
What Is a 1k Ohm Resistor Used For?

A 1k ohm resistor is used in many electronic circuits because it provides a practical current-limiting value for low-voltage designs. It is especially popular in breadboard projects, PCB prototypes, embedded systems, and industrial control boards.

1. LED current limiting

A 1k resistor can limit current through an LED. For example, with a 5V supply and a standard LED, a 1k resistor may allow a small, safe current suitable for indicator lights.

It may not produce maximum brightness, but it is useful when low current consumption is preferred.

2. Pull-up and pull-down circuits

A 1k resistor can help define a digital signal as HIGH or LOW. Pull-up and pull-down resistors prevent floating inputs, which helps microcontrollers read signals more reliably.

In many digital circuits, 1k is considered a stronger pull-up or pull-down value than 10k.

3. Transistor base resistor

A 1k resistor is often used between a microcontroller output and a transistor base. It helps control base current and allows the transistor to switch loads such as LEDs, relays, or small signal circuits.

4. Voltage divider circuits

Two resistors can divide voltage. A 1k resistor may be used with another resistor to create a specific voltage level for analog inputs, reference points, or signal scaling.

5. Signal protection

A 1k resistor can provide simple current limiting for signal lines. It is often placed in series with microcontroller pins, test points, or communication lines to reduce stress during small faults or transitions.

6. PCB testing and debugging

Engineers often use 1k resistors in test circuits because the value is easy to calculate and safe in many low-power conditions.

7. Sensor interface circuits

Some sensors use resistors for biasing, filtering, or signal conditioning. A 1k resistor may be part of a simple RC filter, divider, or output protection path.

What Is a 1k Ohm Resistor Used For?

How to Test a 1k Ohm Resistor?

Testing a 1k resistor is simple with a digital multimeter.

Step 1: Turn off circuit power

Before measuring resistance, make sure the circuit is not powered. Resistance mode should not be used on a live circuit.

Step 2: Set the multimeter to resistance mode

Choose the Ω setting. If your meter has manual range selection, choose a range above 1kΩ, such as 2kΩ or 20kΩ.

Step 3: Touch the probes to both ends

Place one probe on each resistor lead or terminal. Polarity does not matter because resistors are non-polar components.

Step 4: Read the value

A normal 1k resistor should read close to 1000Ω.

Resistor ToleranceAcceptable Reading Range
±1%990Ω to 1010Ω
±2%980Ω to 1020Ω
±5%950Ω to 1050Ω
±10%900Ω to 1100Ω

Step 5: Consider in-circuit measurement

If the resistor is still soldered on a PCB, other nearby components may affect the reading. For the most accurate result, lift one resistor leg or remove the resistor from the circuit.

For SMD resistors, removal may require hot air, tweezers, or a soldering iron. In professional PCBA repair, technicians often compare the measured value with the schematic and surrounding circuit path.

How to Test a 1k Ohm Resistor?

How Much Current Can a 1k Resistor Handle?

The current a 1k resistor can handle depends mainly on its power rating. The resistance value alone is not enough. You need to know whether the resistor is rated for 1/16W, 1/10W, 1/8W, 1/4W, 1/2W, 1W, or higher.

Two useful formulas are:

Power formula:

P = I²R

Current formula:

I = √(P / R)

For a 1k resistor, the maximum current changes with power rating.

Power RatingApproximate Max Current Through 1k Resistor
0.063W / 1⁄16W7.9 mA
0.10W / 1⁄10W10 mA
0.125W / 1⁄8W11.2 mA
0.25W / 1⁄4W15.8 mA
0.50W / 1⁄2W22.4 mA
1.00W31.6 mA

These are theoretical values at full rated power. In real PCB design, engineers usually leave a safety margin. A resistor running at its full rating may become warm and may have reduced long-term reliability.

Voltage also matters. Using Ohm’s law:

V = I × R

For a 1k resistor:

Voltage Across ResistorCurrentPower
3.3V3.3 mA0.0109W
5V5 mA0.025W
12V12 mA0.144W
24V24 mA0.576W

This shows why a 1k resistor works comfortably at 3.3V or 5V in many signal circuits, but may require a higher power rating at 24V.

For example, if a 1k resistor has 24V across it, the power is:

P = V² / R = 24² / 1000 = 0.576W

A small 1/4W resistor would not be suitable for that condition. A higher-rated resistor would be better.

FAQs

1. Is 1k resistor the same as 1000 ohm resistor?

Yes. A 1k resistor is the same as a 1000 ohm resistor. The letter k means kilo, or one thousand. So 1kΩ = 1000Ω.

You may see the same value written as:

  • 1k
  • 1 kΩ
  • 1000Ω
  • 1000R
  • 1.0K

They all refer to the same resistance value.

2. What is the 4-band color code for a 1k resistor?

The 4-band color code for a 1k resistor is usually:

Brown – Black – Red – Gold

Brown is 1, black is 0, red is the multiplier ×100, and gold means ±5% tolerance.

So:

10 × 100 = 1000Ω

If the tolerance is different, the last band may change. For example, brown as the last band means ±1%, while red means ±2%.

3. What is the 5-band color code for a 1k resistor?

The common 5-band color code for a 1k resistor is:

Brown – Black – Black – Brown – Brown

This means:

  • Brown = 1
  • Black = 0
  • Black = 0
  • Brown = ×10
  • Brown = ±1% tolerance

So:

100 × 10 = 1000Ω

This type is often used for precision resistors.

4. Can I use a 1k resistor for LED circuits?

Yes, a 1k resistor can be used for many LED circuits, especially as an indicator LED resistor in 3.3V or 5V circuits.

For example, if you use a 5V supply and a red LED with about 2V forward voltage, the resistor has about 3V across it.

Current is:

I = 3V / 1000Ω = 3 mA

This is safe for many small indicator LEDs. The LED may not be extremely bright, but it is usually bright enough for status indication.

For higher brightness, engineers may choose a lower value such as 330Ω or 470Ω, depending on LED rating, supply voltage, and desired current.

5. How do I know if my 1k resistor is damaged?

You can check a 1k resistor with a multimeter. A healthy resistor should measure close to its rated value.

For example:

  • ±5% 1k resistor: about 950Ω to 1050Ω
  • ±1% 1k resistor: about 990Ω to 1010Ω

A resistor may be damaged if it reads open circuit, far above its rated value, or visually shows burn marks, cracks, discoloration, or damaged leads.

For PCB-mounted resistors, nearby components may affect the reading. If the measured value looks unusual, compare it with the schematic or remove one side of the resistor for a more accurate test.

6. Does resistor tolerance affect 1k resistor value?

Yes. Tolerance tells how much the real value may vary from the marked value.

A 1k resistor with ±5% tolerance can measure between 950Ω and 1050Ω. A 1k resistor with ±1% tolerance can measure between 990Ω and 1010Ω.

For simple LED circuits or general digital circuits, ±5% is often acceptable. For precision measurement, voltage reference, sensor, or analog circuits, ±1% or better may be preferred.

You may also like

What is Silkscreen on PCB? Silkscreen PCB Material & Symbols

May 8th, 2026

What Is Silkscreen on PCB?

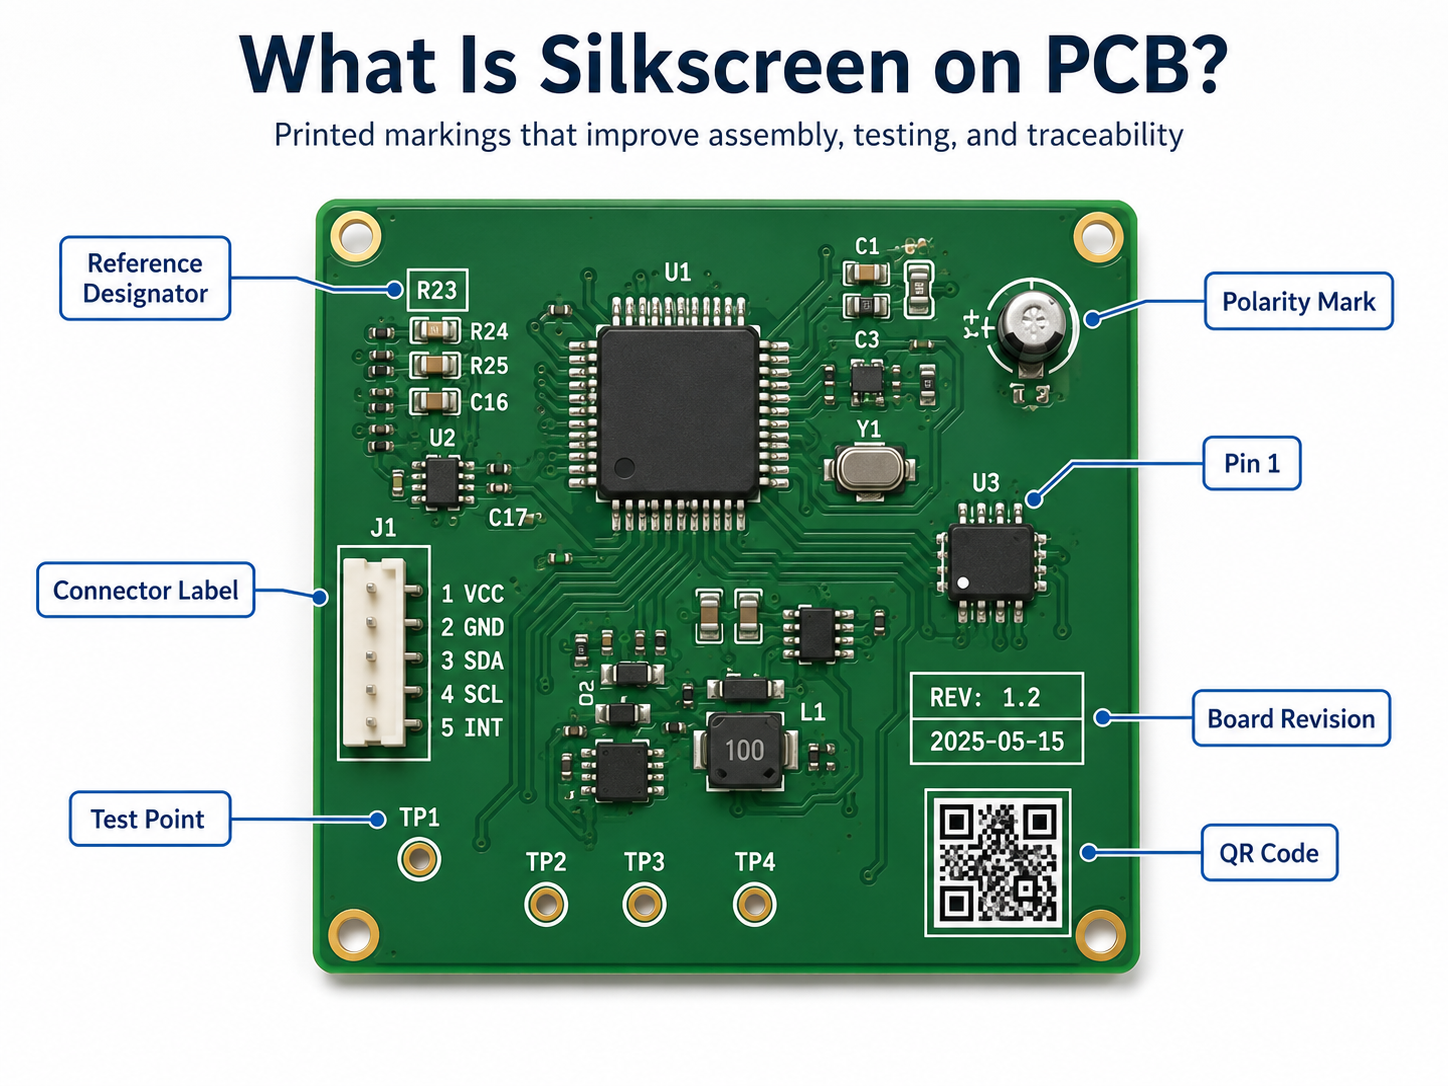
Silkscreen on PCB is the printed marking layer used to show component names, polarity marks, Pin 1 indicators, test points, logos, warning labels, QR codes, and board revision information. It helps engineers, assemblers, inspectors, and repair technicians understand the PCB faster.

This layer is also called the PCB legend layer or component marking layer. It does not carry current, but it plays a practical role in assembly accuracy, testing efficiency, repair work, and product traceability.

What is Silkscreen on PCB? Silkscreen PCB Material & Symbols

Why Is Silkscreen Important on a PCB?

PCB silkscreen is important because it turns a bare circuit board into a readable engineering document. Without silkscreen, the board may still work electrically, but assembly, inspection, testing, and repair become slower.

Clear markings help identify resistors, capacitors, ICs, connectors, test points, power input, signal direction, and safety warnings. In production, a clean silkscreen can reduce orientation mistakes, shorten debugging time, and improve communication between PCB design, fabrication, and assembly teams.

What Is Silkscreen PCB Material?

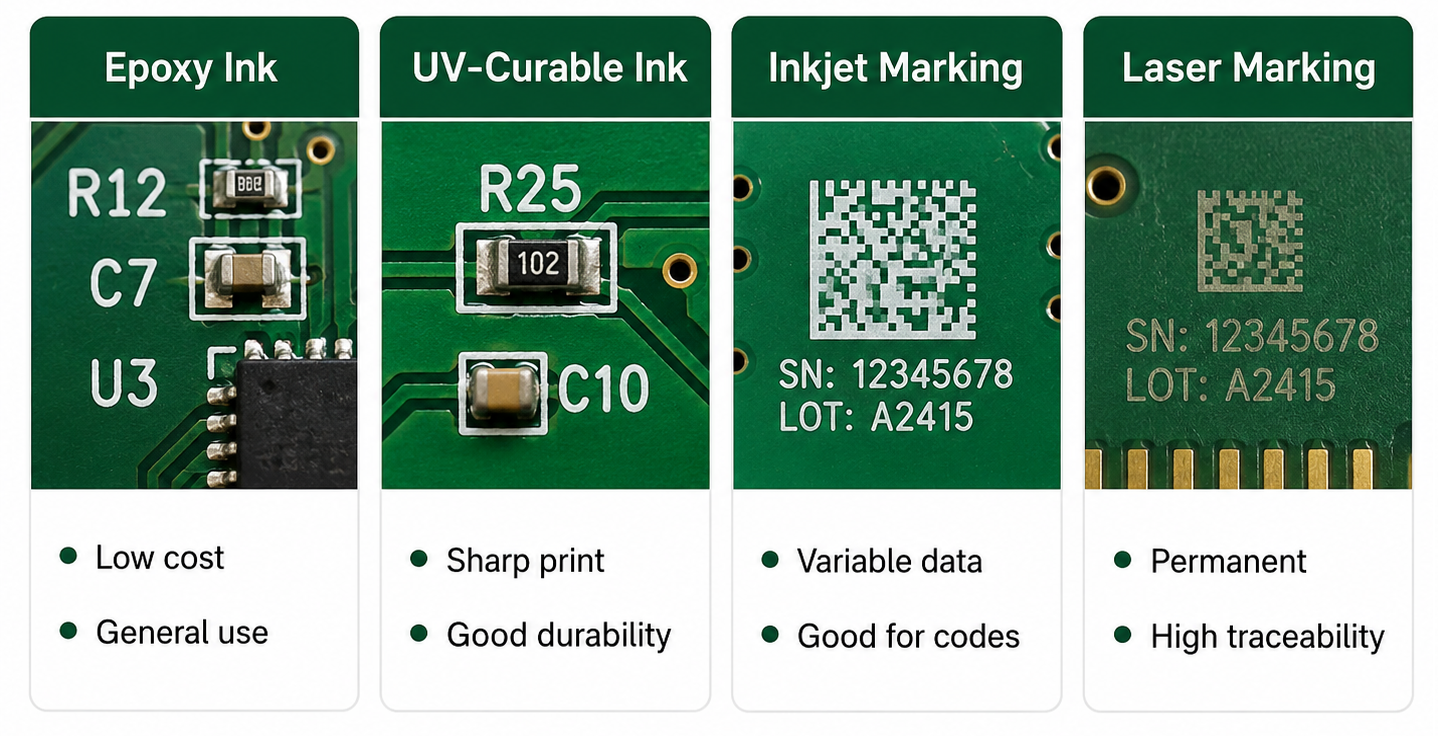
Silkscreen PCB material usually refers to the ink or marking medium used to print text, symbols, and graphics on the PCB surface. The most common material is non-conductive epoxy ink or UV-curable ink. These materials are selected because they can bond to solder mask, resist normal handling, and remain readable after PCB fabrication.

In standard PCB manufacturing, silkscreen material must be compatible with solder mask color, curing temperature, surface finish, cleaning process, and assembly environment. For more demanding products, such as industrial electronics, automotive modules, medical PCBs, or outdoor devices, the marking material should also offer better resistance to abrasion, chemicals, humidity, and temperature changes.

What Are the Common Types of Silkscreen PCB Material?

Different silkscreen PCB material options are used depending on cost, readability, board density, and traceability requirements. Standard epoxy ink is common for most FR4 PCBs. UV-curable ink is used when faster curing and sharper printing are needed. Laser marking is often selected for QR codes, serial numbers, and durable traceability marks.

What Are the Common Types of Silkscreen PCB Material?

For general PCB projects, standard white epoxy or UV ink is enough. For small text, QR codes, high-density boards, or products requiring long-term traceability, higher-resolution printing or laser marking may be a better choice.

How Does Silkscreen PCB Material Affect Readability and Durability?

Silkscreen PCB material affects how sharp, visible, and durable the printed markings are. A good material should keep letters clear after curing, cleaning, soldering, handling, and final assembly.

If the ink spreads too much, small characters may look blurry. If the ink adhesion is weak, markings may fade or scratch off. If the color contrast is poor, technicians may struggle to read the board during inspection or repair.

For example, white silkscreen on green solder mask is easy to read. Black silkscreen on white solder mask also gives strong contrast. But low-contrast combinations, such as gray text on black solder mask, may look stylish while reducing practical readability.

What Are Silkscreen PCB Symbols?

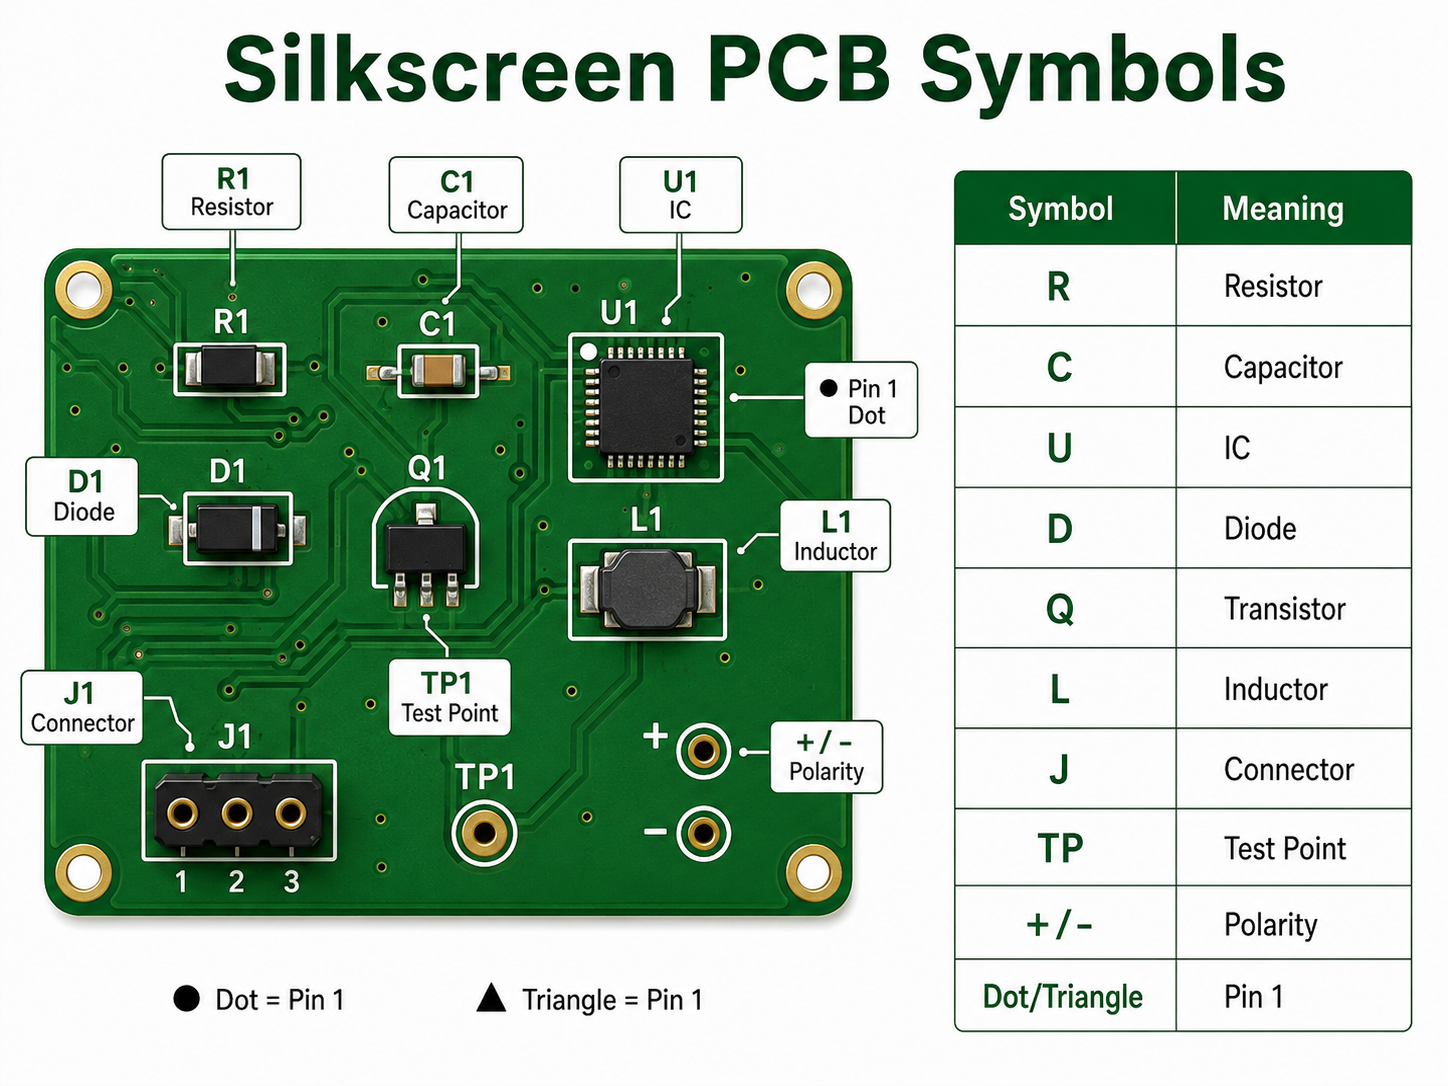
Silkscreen PCB symbols are printed marks used to identify components, polarity, Pin 1 direction, test points, connectors, warning areas, and functional zones on a circuit board. These symbols help users understand the board without opening the schematic every time.

Common silkscreen PCB symbols include “+” and “-” for polarity, dots or triangles for Pin 1, diode bars for cathode direction, TP labels for test points, and reference designators such as R, C, U, D, J, L, Q, and F.

What Do Common Silkscreen PCB Symbols Mean?

What Do Common Silkscreen PCB Symbols Mean?
Silkscreen PCB SymbolMeaningExample
RResistorR1, R25
CCapacitorC3, C18
U / ICIntegrated circuitU1, IC2
DDiode or LEDD5, LED1
QTransistor or MOSFETQ2, Q10
LInductorL1, L4
J / CNConnectorJ1, CN3
FFuseF1
TPTest pointTP1, TP_GND
SWSwitchSW1
+ / –PolarityCapacitor, battery, LED
Dot / triangle / “1”Pin 1 indicatorIC or connector orientation
GNDGroundGround test point
VIN / VOUTPower input/outputPower connector marking
HVHigh voltage warningPower supply board

These silkscreen PCB symbols are small, but they carry important information. A missing polarity mark or unclear Pin 1 indicator can cause assembly errors, especially on LED boards, power supplies, sensor modules, and control boards.

How Do Silkscreen PCB Symbols Help Assembly?

Silkscreen PCB symbols help assembly teams place and inspect components correctly. They show where each component belongs, which direction it should face, and how connectors or test points should be used.

For SMT assembly, symbols such as Pin 1 dots, diode direction marks, and capacitor polarity marks are very useful during first article inspection. For through-hole assembly, connector names, switch labels, and power marks help manual operators avoid wrong insertion.

In PCBA production, clear symbols can support:

  • Faster visual inspection
  • Lower risk of component orientation errors
  • Easier connector installation
  • Better manual soldering guidance
  • Faster functional testing
  • Easier repair and troubleshooting

What Are the Design Rules for Silkscreen on PCB?

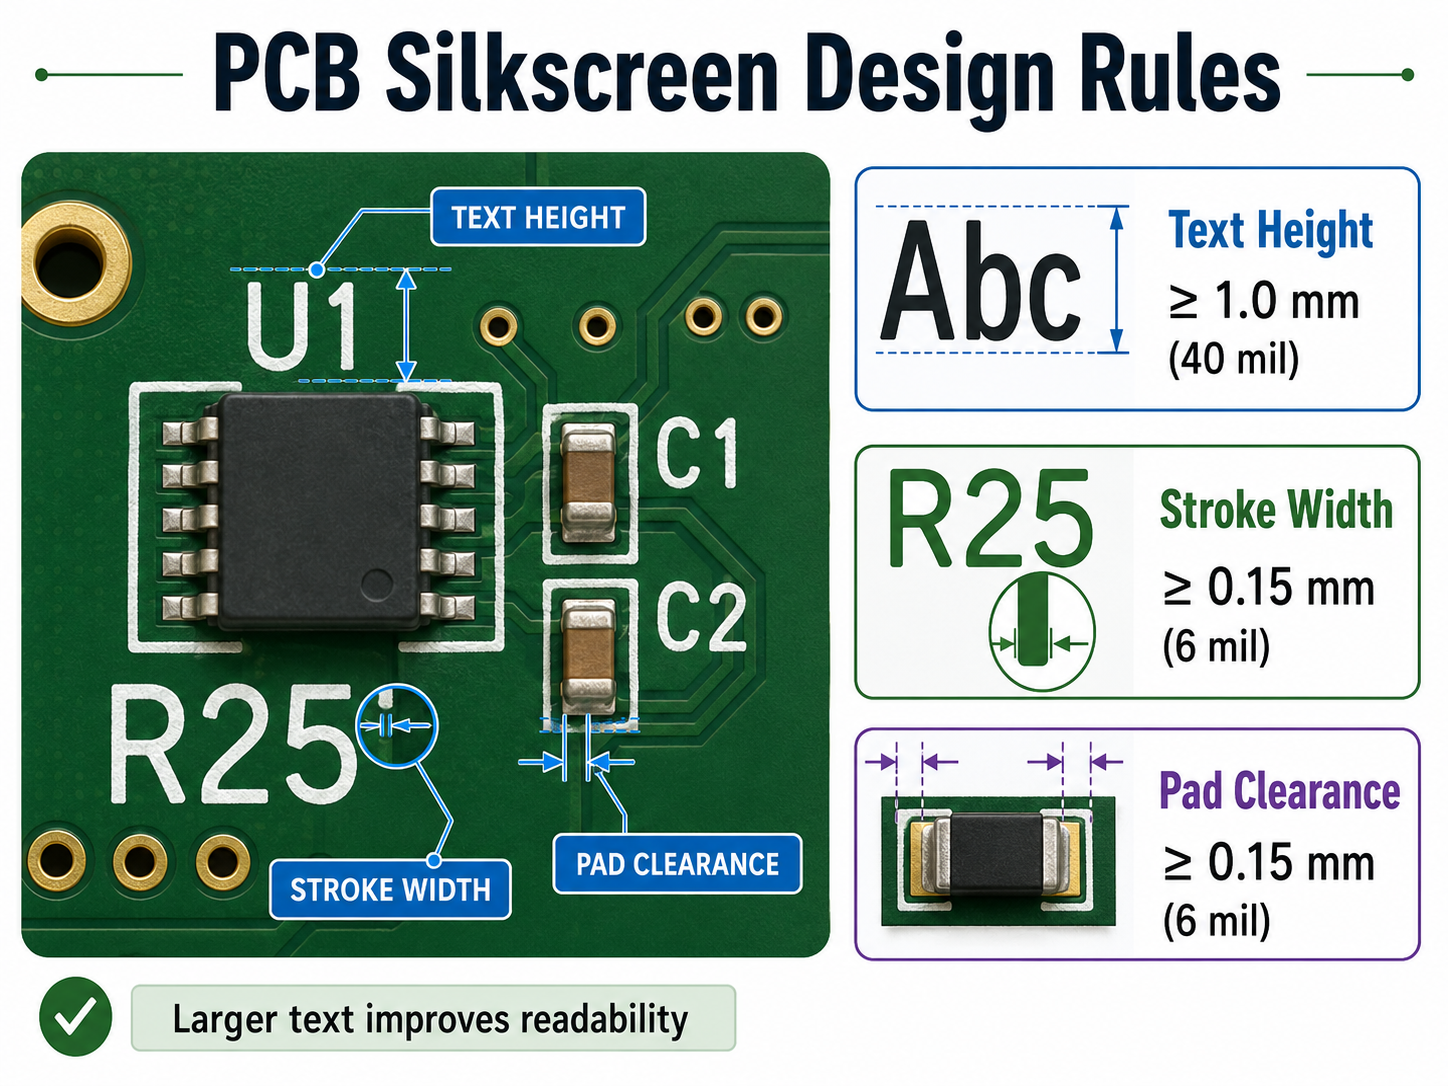
Silkscreen on PCB should be designed with enough character size, stroke width, and clearance from pads. The markings must remain readable after fabrication and assembly.

Design ItemRecommended Value
Text height≥1.0 mm / 40 mil
Stroke width≥0.15 mm / 6 mil
Clearance to pads≥0.15 mm / 6 mil
Clearance to exposed copper≥0.15 mm / 6 mil
Hollow font height≥1.5 mm / 60 mil
QR code sizeConfirm with supplier
Bottom-side textMirrored correctly

If the board is very dense, do not force every component label onto the PCB. Keep important markings first: Pin 1, polarity, test points, connector names, warning labels, and revision number.

Can Silkscreen Be Printed Over Pads or Vias?

Silkscreen should not be printed over solder pads, exposed copper, gold fingers, test points, or solderable vias. If silkscreen overlaps these areas, the PCB manufacturer may remove part of the text during CAM processing.

This is why some letters disappear after fabrication. The original design may show complete text, but the manufacturing file may clip it to protect soldering quality.

A better practice is to place reference designators outside component bodies and away from pads. For small components, use shorter labels or place the full reference information in the assembly drawing.

What Is the Difference Between Silkscreen PCB Material and Solder Mask Material?

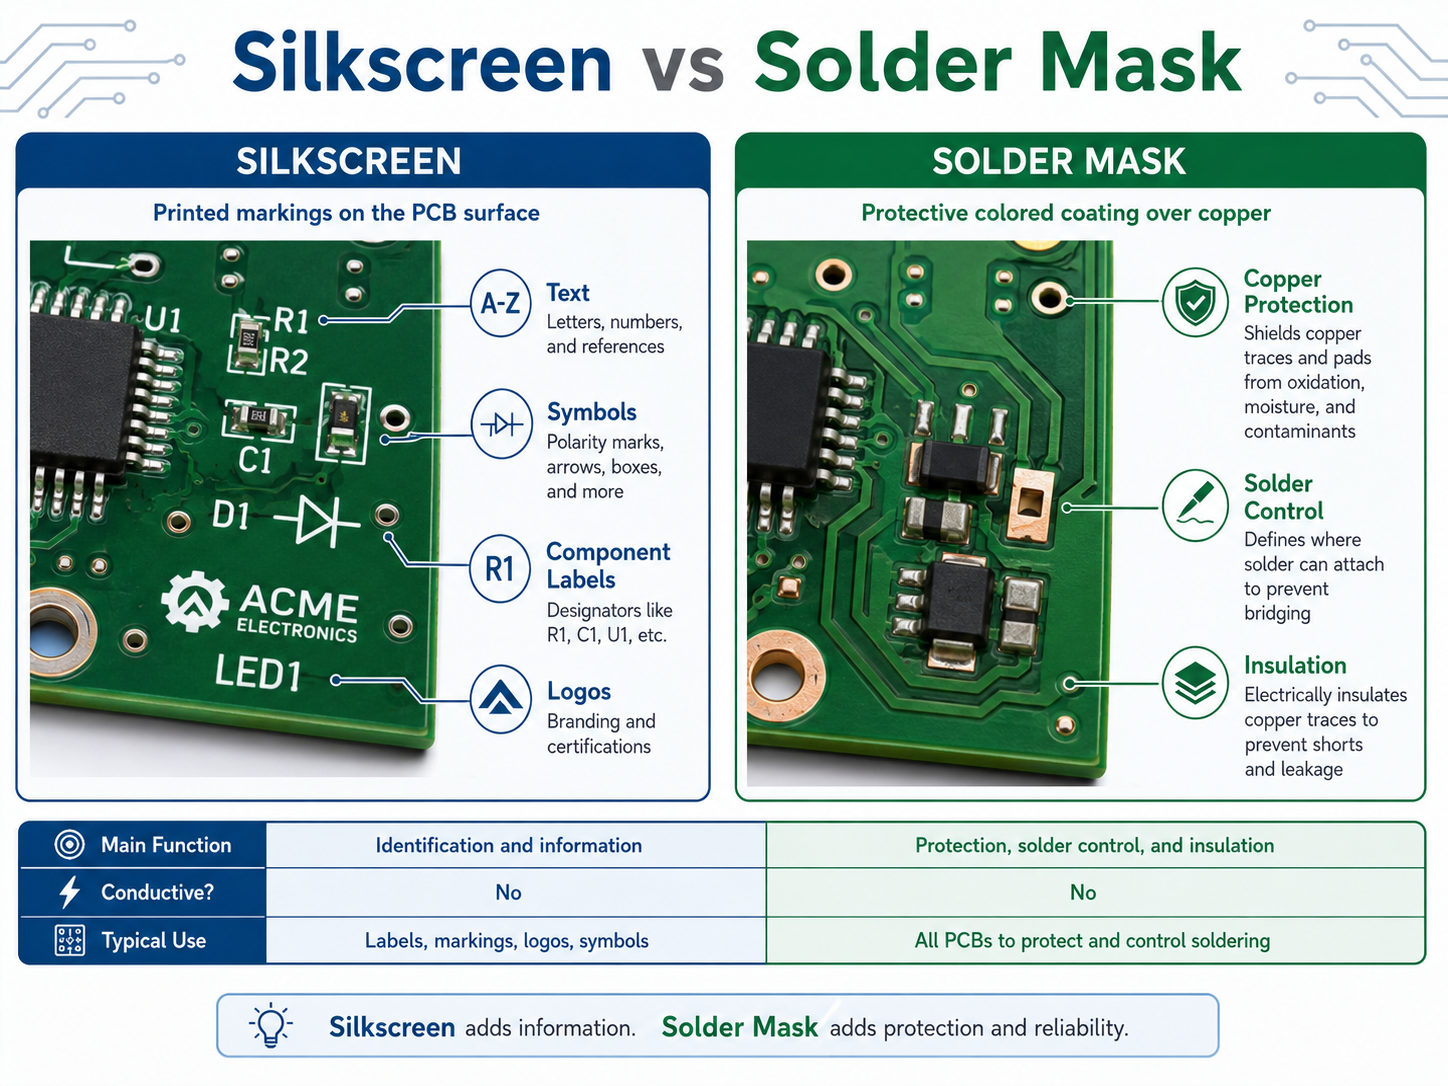
Silkscreen PCB material is used for printed markings. Solder mask material is used to protect copper and prevent solder bridges. They are different layers with different functions.

ItemSilkscreen PCB MaterialSolder Mask Material
Main functionPrints text, symbols, and logosCovers and protects copper
Electrical roleNon-conductive markingInsulating protection
Common colorWhite, black, yellowGreen, black, blue, red, white
Used forComponent labels, symbols, warningsSolder control and copper protection
Design concernReadability and clearanceInsulation and solderability

A PCB needs solder mask for manufacturing protection. Silkscreen is used for human readability. Both layers support production quality, but they should not be confused.

How Should You Choose Silkscreen PCB Material and Color?

Choose silkscreen PCB material and color based on readability, product environment, board density, and traceability needs. For most PCB projects, white silkscreen on green solder mask is the safest and most readable choice.

For white solder mask, black silkscreen is usually better. For black solder mask, white silkscreen gives better contrast. For products with QR codes, serial numbers, or long-term tracking needs, laser marking or high-resolution legend printing may be more reliable.

PCB Solder Mask ColorRecommended Silkscreen ColorReadability
GreenWhiteExcellent
BlueWhiteExcellent
RedWhiteGood
BlackWhiteGood
WhiteBlackExcellent
YellowBlackGood

For industrial, medical, automotive, and communication products, readability should be more important than visual decoration. A beautiful board is helpful, but a readable board is more useful in production and maintenance.

How Can EBest Circuit Help With PCB Silkscreen Design and Manufacturing?

EBest Circuit can help review silkscreen on PCB before fabrication and assembly. Our team checks text size, symbol clarity, polarity marks, Pin 1 indicators, pad clearance, QR code position, and board revision information during DFM review.

This is especially useful for turnkey PCB and PCBA projects. Silkscreen is not only a printing detail. It connects with BOM verification, component orientation, assembly inspection, testing, traceability, and repair documentation.

EBest Circuit supports:

  • PCB fabrication
  • PCBA assembly
  • Component sourcing
  • Free DFM review
  • Silkscreen readability check
  • QR code and serial number marking
  • AOI, X-ray, ICT, and functional testing
  • Prototype to mass production support

For projects that require clean markings, stable assembly, and traceable manufacturing, send your Gerber and BOM files to sales@bestpcbs.com.

FAQs

1. What is silkscreen on PCB?

Silkscreen on PCB is the printed marking layer that shows component names, symbols, polarity, test points, logos, QR codes, and board revision information. It helps people assemble, test, inspect, and repair the PCB more easily.

2. What material is used for PCB silkscreen?

Common silkscreen PCB material includes epoxy-based ink, UV-curable ink, LPI legend ink, inkjet marking ink, or laser marking depending on the required precision, durability, and traceability.

3. What do silkscreen PCB symbols mean?

Silkscreen PCB symbols identify components and board functions. For example, R means resistor, C means capacitor, U means IC, D means diode, TP means test point, and “+ / -” shows polarity.

4. Does silkscreen PCB material affect circuit performance?

Normally, no. Silkscreen material is non-conductive and does not carry current. However, poor placement over pads, exposed copper, or sensitive areas can create manufacturing or readability problems.

5. Can PCB silkscreen symbols be customized?

Yes. Custom symbols, logos, connector labels, warning marks, QR codes, and product IDs can be printed on the PCB as long as they meet the manufacturer’s minimum size and clearance rules.

6. What is the best silkscreen color for PCB?

White is the most common silkscreen color because it gives strong contrast on green, blue, red, and black solder mask. Black silkscreen is usually better for white solder mask.

You may also like

What is Silkscreen on PCB? Clear Marking for Better Assembly

May 8th, 2026

What Is Silkscreen on PCB?

Silkscreen on PCB is the printed layer of text, symbols, logos, reference designators, polarity marks, test points, warning signs, and revision information placed on the surface of a printed circuit board. It does not conduct electricity. Its main job is to help people read, assemble, test, repair, and trace the board more easily.

On most circuit boards, the silkscreen is the white text you see on top of a green solder mask. However, it can also be black, yellow, gray, or another color depending on the PCB surface color and manufacturing process.

What Is Silkscreen on PCB?

What Is the Main Purpose of PCB Silkscreen?

The main purpose of PCB silkscreen is to make the board easier to identify, assemble, inspect, test, and maintain. It gives visible information to people working with the board during production and after the product enters the field.

A good silkscreen design usually includes component names, polarity marks, Pin 1 indicators, connector labels, test point numbers, warning text, board revision, and company logo. These small details can make a large difference during real production.

Common uses include:

  • Identifying resistors, capacitors, ICs, diodes, connectors, and switches
  • Showing polarity for LEDs, diodes, electrolytic capacitors, and batteries
  • Marking Pin 1 on ICs, headers, flat cables, and connectors
  • Labeling test points for ICT, flying probe, or functional testing
  • Adding board name, part number, revision, date code, or QR code
  • Warning users about high voltage, hot surfaces, ESD-sensitive zones, or orientation requirements
  • Supporting repair and field maintenance

What Information Should Be Included on a PCB Silkscreen?

A useful PCB silkscreen should include only the information that helps assembly, testing, inspection, traceability, and maintenance. The goal is not to print everything possible. The goal is to print the right information in the right place.

For simple boards, it is common to include every reference designator, such as R1, C1, U1, D1, and J1. For high-density boards, space may be limited, so designers should prioritize information that prevents mistakes.

The most important silkscreen items usually include:

Silkscreen ItemExample
Reference designatorR12, C8, U3, J1
Polarity mark+, -, cathode line
Pin 1 markDot, triangle, “1”
Connector labelUSB, VIN, OUT, CANH
Test point labelTP1, GND, 3V3, RESET
Board revisionREV A, V1.2
Manufacturing codeDate code, lot number
QR code or serial numberProduct ID, batch ID
Warning markHIGH VOLTAGE, HOT
Logo or brand nameEBest, customer logo

For many products, the highest-priority marks are polarity, Pin 1, connector direction, test points, and board revision. These markings are closely tied to assembly accuracy and maintenance efficiency.

What Is the Difference Between Silkscreen and Solder Mask?

Silkscreen and solder mask are different PCB layers. Solder mask is a protective coating that covers copper and helps control soldering. Silkscreen is a printed marking layer used for text, symbols, logos, and identification.

The solder mask is usually the colored background, such as green, black, blue, red, or white. The silkscreen is the printed legend on top of that surface.

Silkscreen vs Solder Mask

For high-reliability electronics, such as medical devices, industrial controls, aerospace modules, automotive boards, and communication equipment, both layers should be reviewed carefully during DFM checking.

What Are the Standard PCB Silkscreen Design Rules?

Standard PCB silkscreen design rules focus on readability, manufacturability, and clearance. The markings should be large enough to read, thick enough to print, and far enough from pads, exposed copper, and component bodies.

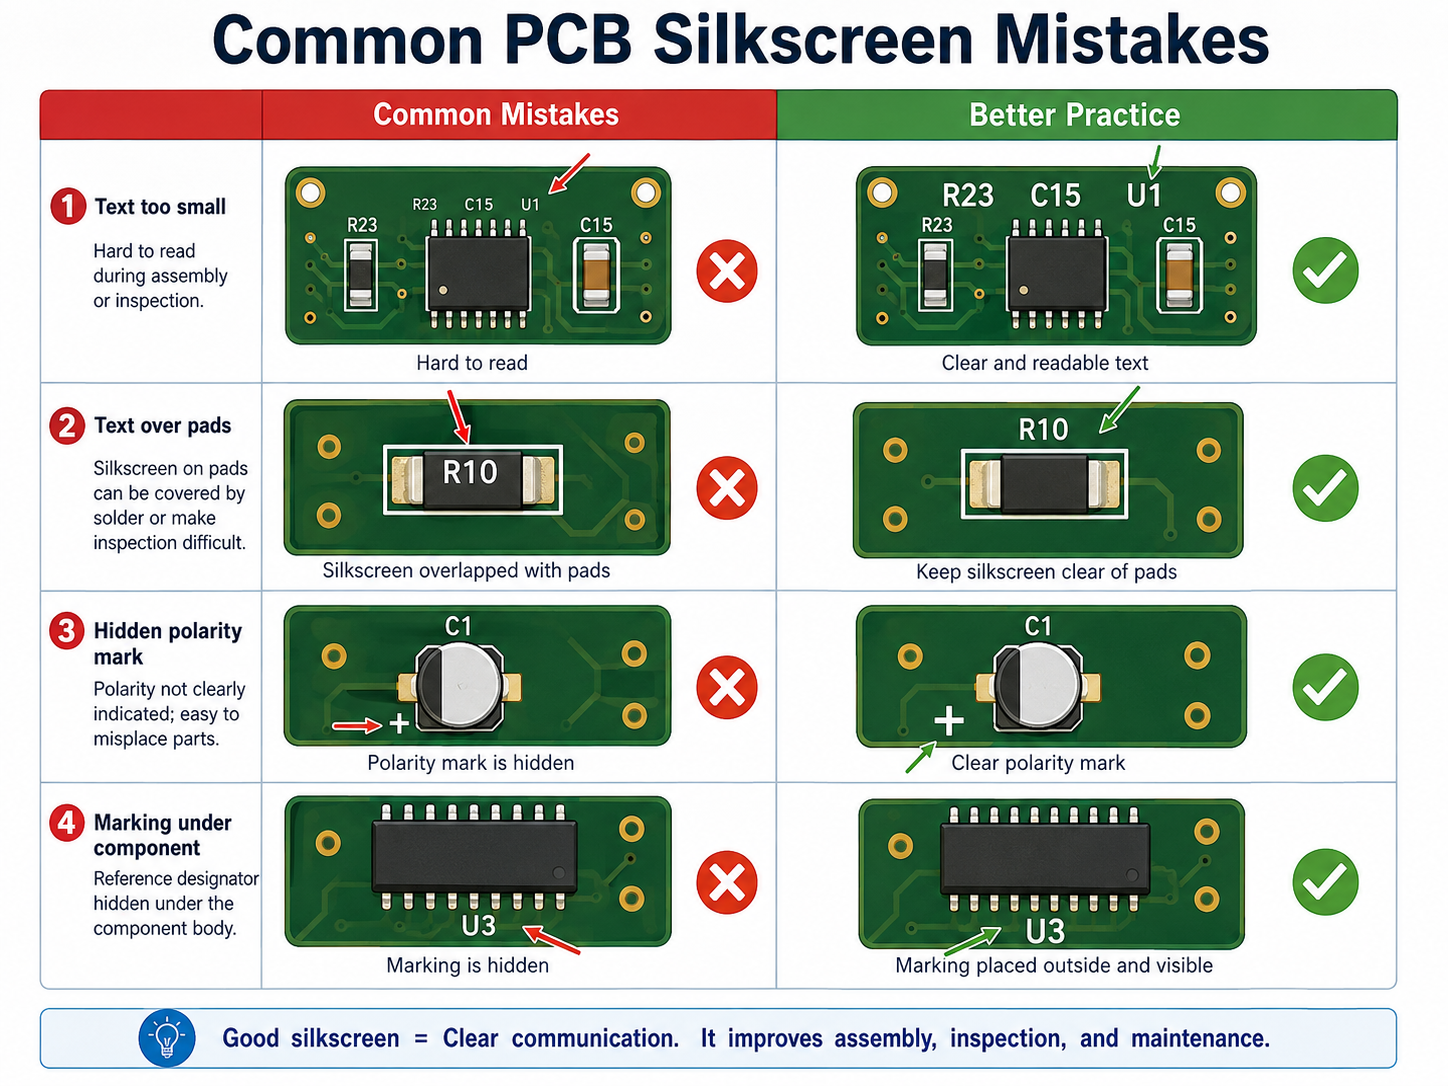
A common mistake is designing silkscreen text that looks clear in CAD software but becomes too small after fabrication. Another common issue is placing text too close to solder pads. During CAM processing, the PCB factory may clip or remove part of the silkscreen to avoid pad contamination.

The following table gives practical reference values for standard PCB projects.

Design ItemRecommended ValueBetter Practice
Text height≥1.0 mm / 40 mil1.27 mm / 50 mil
Stroke width≥0.15 mm / 6 mil0.18–0.20 mm / 7–8 mil
Clearance to solder pad≥0.15 mm / 6 mil≥0.20 mm / 8 mil
Clearance to exposed copper≥0.15 mm / 6 mil≥0.20 mm / 8 mil
Hollow text height≥1.5 mm / 60 mil≥2.0 mm / 80 mil
Hollow text stroke≥0.20 mm / 8 mil≥0.25 mm / 10 mil
QR code sizeDepends on data amountConfirm with manufacturer
Bottom textMirrored in layoutVerify in Gerber viewer

These values are practical for many standard FR4 boards. However, each PCB manufacturer may have different process capability. Fine-pitch HDI boards, ceramic PCBs, metal core PCBs, and high-frequency boards may need a separate review.

What Is the Minimum Text Size for Silkscreen on PCB?

For a reliable and readable PCB silkscreen, a text height of at least 1.0 mm and a stroke width of at least 0.15 mm are commonly recommended. If the board has enough space, larger text is better for manual inspection, testing, and repair.

Here is a useful conversion table for PCB silkscreen design:

Metric SizeApprox. Imperial SizeCommon Use
0.15 mm5.9 milMinimum practical stroke width
0.18 mm7.1 milMore stable stroke width
0.20 mm7.9 milBetter for normal production
0.80 mm31.5 milSmall text, limited readability
1.00 mm39.4 milStandard readable text height
1.27 mm50.0 milBetter manual readability
1.50 mm59.1 milGood for labels and warnings
2.00 mm78.7 milGood for connectors or safety text

Can Silkscreen Be Printed Over Pads, Vias, or Copper?

Silkscreen should not be printed over solder pads, exposed copper, gold fingers, test pads, or solderable via areas. If the marking overlaps these areas, the factory may remove it during CAM processing. In some cases, poor placement can also affect appearance or assembly readability.

Silkscreen ink is usually non-conductive, but that does not mean it should be placed anywhere. Pads and exposed copper need clean surfaces for soldering, testing, or electrical contact. When silk markings are too close to these areas, the result may be missing text, cut letters, or unclear symbols.

Designers should pay extra attention to these areas:

  • SMT pads
  • Through-hole pads
  • Test points
  • Exposed copper zones
  • Gold fingers
  • Castellated holes
  • Thermal pads
  • High-current terminals
  • RF launch areas
  • Fine-pitch IC footprints

What Are Common PCB Silkscreen Mistakes?

Common PCB silkscreen mistakes include using text that is too small, placing marks under components, printing over pads, forgetting polarity marks, using unclear symbols, and failing to check bottom-side mirroring.

The most common PCB silkscreen mistake including:

What Are Common PCB Silkscreen Mistakes?

What Colors Are Common for PCB Silkscreen?

White is the most common PCB silkscreen color because it gives strong contrast on green, red, blue, and black solder masks. Black silkscreen is common on white solder mask or light-colored boards. Yellow, gray, and other colors may be available depending on the manufacturer.

Color is not only an appearance choice. It affects readability. For example, white text on a green solder mask is easy to read, black text on a white solder mask also gives good contrast. Gray text on a black board may look stylish, but it may be less readable during repair or inspection.

Common color combinations include:

Solder Mask ColorCommon Silkscreen ColorReadability
GreenWhiteExcellent
BlueWhiteExcellent
RedWhiteGood
BlackWhiteGood
WhiteBlackExcellent
YellowBlackGood
Matte blackWhite or light grayGood
Transparent / no maskDepends on copper finishRequires review

If the PCB will go through conformal coating, potting, cleaning, or harsh field use, confirm whether the marking remains visible after the final process. The best silkscreen design considers the full product lifecycle, not only the bare board.

How Can a PCB Manufacturer Improve Silkscreen Quality?

A reliable PCB manufacturer improves silkscreen quality through DFM review, proper printing process selection, CAM checking, readable text control, and clear communication before production. The best result comes from both good design and disciplined manufacturing.

Silkscreen quality depends on several factors:

  • Ink type
  • Printing method
  • Solder mask surface
  • Character size
  • Stroke width
  • Board material
  • Surface finish
  • Curing process
  • CAM clearance rules
  • Operator and equipment control

For standard PCBs, traditional silkscreen printing is often sufficient. For dense layouts, QR codes, small text, or high-end appearance, direct legend printing, inkjet printing, or laser marking may be a better option.

EBest Circuit supports PCB fabrication, PCBA assembly, component sourcing, testing, and engineering review for prototype and production projects. For silkscreen-related issues, our team can help check text size, polarity marks, Pin 1 indicators, reference designators, QR code areas, and manufacturing readability before production starts.

How Do You Design Better Silkscreen for High-Density PCBs?

For high-density PCBs, silkscreen should be selective, not crowded. When there is not enough room, keep only the markings that prevent assembly mistakes and support testing. Other information can be moved to the assembly drawing or digital documentation.

A better priority order is:

  • Pin 1 marks for ICs and connectors
  • Polarity marks for LEDs, diodes, capacitors, and battery connectors
  • Test point labels for production and repair
  • Connector function labels
  • Board revision and traceability marks
  • Selected reference designators for important components
  • Logo and non-essential graphics

For very small boards, use simple but clear symbols. A small dot for Pin 1, a cathode bar for diode orientation, or a “+” mark for positive polarity can be more valuable than long text.

pcb silkscreen design rules

How Should You Work With a Manufacturer on PCB Silkscreen?

To get a clean silkscreen result, provide complete manufacturing files and ask the PCB manufacturer to review the marking layer before fabrication. This is especially important for dense boards, double-sided assembly, QR code marking, medical electronics, industrial products, and high-reliability applications.

Send these files when possible:

  • Gerber files
  • Drill file
  • PCB stackup
  • Assembly drawing
  • BOM
  • Pick-and-place file
  • Special marking requirements
  • QR code or serial number rule
  • Preferred silkscreen color
  • Any customer logo file
  • Required board revision format

Before production, confirm these points:

  • Is the text size manufacturable?
  • Is the stroke width stable?
  • Is the silkscreen clear from pads and exposed copper?
  • Are Pin 1 and polarity marks visible after assembly?
  • Will the QR code scan after printing?
  • Is the board revision correct?
  • Is bottom-side text mirrored correctly?
  • Will coating, cleaning, or final assembly hide any marks?

For customers who need PCB fabrication and assembly together, EBest Circuit can review silkscreen together with component placement, BOM, test access, and assembly process. This helps prevent small marking issues from becoming production delays.

FAQs About Silkscreen on PCB

1. Is silkscreen on PCB necessary?
Yes, it is highly useful. A PCB can work electrically without silkscreen, but clear markings make assembly, testing, inspection, repair, and traceability much easier. For production boards, it is strongly recommended.

2. Does PCB silkscreen affect circuit performance?
In normal designs, it does not affect electrical performance because the ink is non-conductive. Still, it should be kept away from solder pads, exposed copper, RF-sensitive areas, high-voltage clearances, and test contact areas.

3. What is the best font size for PCB silkscreen?
A practical choice is at least 1.0 mm text height with 0.15 mm stroke width. If the board has enough space, 1.27 mm text height and 0.18–0.20 mm stroke width offer better readability.

4. Can I print a logo on PCB silkscreen?
Yes. Logos are commonly printed on PCB silkscreen. The logo should meet minimum line width and spacing rules. It should also avoid pads, exposed copper, QR codes, and important technical markings.

5. Can silkscreen include QR codes or serial numbers?
Yes. QR codes, serial numbers, lot codes, and product IDs can be added to support traceability. For small or high-density codes, laser marking or high-resolution printing may be more reliable than standard silkscreen.

6. Why did some silkscreen text disappear after PCB production?
The most common reason is that the text overlapped pads, vias, exposed copper, or restricted areas. During CAM processing, the factory may remove part of the marking to protect solderability and manufacturing quality.

7. What is the difference between PCB silkscreen and PCB legend?
They usually refer to the same idea. “Silkscreen” often describes the printed marking process, while “legend” refers to the text and symbols shown on the PCB surface.

8. Which silkscreen color is best for PCB?
White is the most common choice because it works well on green, blue, red, and black solder masks. Black is better for white solder mask. The best color is the one that gives strong contrast and stable readability.

Conclusion

Silkscreen on PCB may look like a small detail, but it has a practical role in the full product lifecycle. It helps assemblers place components correctly, helps testers find signals quickly, helps repair teams locate parts, and helps manufacturers support traceability.

EBest Circuit provides PCB fabrication, PCBA assembly, component sourcing, DFM review, and testing support for prototype and mass production projects. If your PCB needs clear silkscreen, reliable assembly, and traceable production, send your Gerber and BOM files to our team for review.

Contact EBest Circuit: sales@bestpcbs.com

You may also like

What is a High Reliability Circuit Board and How Does It Differ from Standard Ones?

May 8th, 2026

What makes a high reliability circuit board essential for critical applications? It endures extreme conditions and meets strict standards, making it irreplaceable in key industries. Many engineers struggle with its key elements. This guide helps navigate its design, materials and testing.

High Reliability Circuit Board, https://www.bestpcbs.com/blog/2026/05/high-reliability-circuit-board/

What is a High Reliability Circuit Board?

A high reliability circuit board is a specialized printed circuit board designed to maintain consistent performance and durability in harsh or critical environments where failure could lead to safety risks, significant financial losses, or operational downtime. Unlike standard boards, high reliability printed circuit boards undergo stricter design, material selection, manufacturing, and testing processes to ensure they can withstand extreme temperatures, vibration, humidity, chemical exposure, and long-term use without degradation.

High reliability board are used in applications where performance is non-negotiable, such as aerospace, defense, medical devices, industrial automation, and automotive safety systems. These boards are engineered to meet specific reliability metrics, including mean time between failures (MTBF), thermal stability, and mechanical robustness. The core goal of a high reliability PCB is to eliminate potential points of failure, from component placement to solder joints, ensuring the board operates as intended for its entire service life.

Multilayer PCB fabrication plays a key role in creating high reliability circuit boards, as multilayer designs allow for greater component density, improved signal integrity, and better thermal management, all critical for reliability in complex systems. Multilayer PCB fabrication enables engineers to design boards that fit into compact spaces while maintaining the durability needed for harsh environments, making it a cornerstone of high reliability printed circuit boards manufacturing.

What Are the Differences Between High Reliability Circuit Board and Standard Circuit Board?

Understanding the distinctions between high reliability circuit boards and standard ones is crucial for selecting the right board for your application. These differences span materials, manufacturing, testing, and performance, directly impacting how well the board can meet your project’s requirements. Below is a detailed comparison to clarify their unique characteristics.

CategoryHigh Reliability Circuit BoardsStandard Circuit Boards
Material QualityUse high-grade materials such as FR-4 with high Tg (glass transition temperature), polyimide, or Rogers materials for thermal and mechanical stability. Materials are rigorously tested for consistency and durability.Use standard FR-4 or low-grade materials with lower Tg. Materials are selected for cost-effectiveness rather than long-term reliability.
Manufacturing TolerancesStrict manufacturing tolerances for trace width, spacing, hole size, and layer alignment. Multilayer PCB fabrication for high reliability uses precise lamination processes to ensure layer adhesion and minimize defects.Wider manufacturing tolerances to reduce costs. Multilayer PCB fabrication (when used) uses basic lamination processes with less quality control.
Testing RequirementsComprehensive testing including thermal cycling, vibration testing, humidity testing, X-ray inspection, and continuity testing. Every board may undergo 100% inspection to ensure no defects.Basic testing such as visual inspection and continuity checks. Random sampling is common, and many defects may go undetected.
Design FocusDesigned for thermal management, signal integrity, and mechanical robustness. Multilayer PCB fabrication is often used to optimize these factors, with careful consideration of component placement and trace routing.Designed for cost-effectiveness and basic functionality. Little focus on thermal management or signal integrity beyond basic requirements.
Application Use CasesAerospace, defense, medical devices, industrial automation, automotive safety systems, and other critical applications where failure is catastrophic.Consumer electronics, toys, basic appliances, and other non-critical applications where occasional failure is acceptable.
Service LifeEngineered for long service life (10+ years) with minimal degradation. Multilayer PCB fabrication enhances durability, ensuring the board withstands long-term use in harsh conditions.Service life is typically 2-5 years, with degradation expected over time due to lower-quality materials and manufacturing.

What Design Principles Should Be Followed for High Reliability PCB Design?

Designing a high reliability PCB requires more than basic circuit layout, it demands intentional choices to enhance durability, signal integrity, and thermal performance. The following principles are foundational to creating boards that can withstand harsh conditions and deliver long-term reliability.

  • Prioritize Thermal Management: High reliability PCB generate heat during operation, so design must include heat sinks, thermal vias, and proper component placement to dissipate heat. Multilayer PCB fabrication allows for dedicated thermal layers to distribute heat evenly, preventing overheating and component failure. Ensure components with high heat output are placed away from heat-sensitive parts and use materials with high Tg to resist thermal expansion.
  • Optimize Signal Integrity: Signal degradation can lead to board failure, so design traces to minimize noise, crosstalk, and impedance mismatch. Use controlled impedance traces, separate analog and digital signals, and keep high-speed traces short. Multilayer PCB fabrication enables signal layers to be isolated from power and ground layers, reducing interference and improving signal integrity.
  • Mechanical Robustness: Design the board to withstand vibration, shock, and physical stress. Use thicker copper layers for mechanical strength, avoid sharp corners on traces, and ensure proper mounting points. Multilayer PCB fabrication with strong lamination bonds enhances the board’s mechanical stability, making it resistant to bending and warping.
  • Redundancy and Fault Tolerance: Incorporate redundant components or pathways to ensure the board continues functioning if one component fails. This is critical for high reliability board used in critical applications such as medical devices and aerospace systems. Redundancy design should be integrated early in the process, with multilayer PCB fabrication allowing for compact placement of redundant components.
  • Component Selection: Choose components rated for high reliability, including extended temperature ranges, low failure rates, and compliance with industry standards. Avoid counterfeit or low-grade components, as they are a common source of board failure. Components should be compatible with the board’s material and manufacturing processes, including multilayer PCB fabrication requirements.
  • Controlled Impedance: Maintain consistent impedance across traces to ensure signal integrity, especially for high-speed applications. Use impedance calculators to determine trace width and spacing, and verify impedance during manufacturing. Multilayer PCB fabrication allows for precise control of trace dimensions, ensuring consistent impedance throughout the board.
High Reliability PCB Design, https://www.bestpcbs.com/blog/2026/05/high-reliability-circuit-board/

How to Ensure Quality in High-Reliability Circuit Board Assembly Processes?

Even the best-designed high reliability PCB can fail if assembly processes are not carefully controlled. Quality assurance at every step of assembly is key to preventing defects and ensuring the board meets its reliability standards. Here’s how to maintain quality during assembly.

  • Strict Material Inspection: Inspect all raw materials, including PCB substrates, copper foils, solder paste, and components, before assembly. Verify material specifications, including Tg, thermal conductivity, and mechanical properties. For multilayer PCB fabrication, inspect each layer before lamination to ensure no defects or contamination.
  • Precision Solder Paste Application: Use automated solder paste printers with high accuracy to ensure consistent paste volume and placement. Solder paste should be stored and handled according to manufacturer guidelines to prevent degradation. Proper paste application is critical for strong solder joints, which are essential for high reliability board performance.
  • Controlled Reflow Soldering: Use reflow ovens with precise temperature control to ensure solder joints are formed correctly. Follow a carefully calibrated reflow profile to avoid cold joints, bridging, or component damage. For high reliability PCB, reflow processes should be monitored and documented to ensure consistency.
  • Automated Optical Inspection (AOI): Use AOI systems to inspect solder joints, component placement, and board defects after assembly. AOI can detect issues such as missing components, misalignment, and solder bridging that may be missed by visual inspection. This step is critical for ensuring high reliability in mass-produced boards.
  • X-Ray Inspection: For multilayer PCB fabrication and boards with hidden components (such as BGA packages), use X-ray inspection to verify solder joint quality and layer alignment. X-ray inspection can detect internal defects, such as voids in solder joints, which can compromise reliability.
  • Environmental Testing After Assembly: Subject assembled boards to environmental testing, including thermal cycling, humidity testing, and vibration testing, to simulate real-world conditions. This ensures the board can withstand harsh environments without failure. Testing results should be documented and used to improve assembly processes.
  • Quality Control Documentation: Maintain detailed records of all assembly processes, including material inspections, solder paste application, reflow profiles, and testing results. Documentation ensures traceability and allows for root cause analysis if defects are found. This is essential for compliance with industry standards for high reliability printed circuit boards.

What Are the Materials for Manufacturing High Reliability Printed Circuit Boards?

The materials used in high reliability printed circuit boards directly influence their performance and durability. Choosing the right substrates, conductors, and auxiliary materials is essential for withstanding extreme conditions and meeting industry standards. Below are the key materials for manufacturing these specialized boards.

  • High-Tg FR-4: The most common material for high reliability PCB, high-Tg FR-4 (glass transition temperature above 170°C) offers excellent thermal stability, mechanical strength, and electrical insulation. It is suitable for most high reliability applications and is compatible with standard multilayer PCB fabrication processes. High-Tg FR-4 resists warping and degradation at high temperatures, making it ideal for industrial and automotive applications.
  • Polyimide (PI): A high-performance material with exceptional thermal resistance (Tg above 250°C), chemical resistance, and mechanical flexibility. Polyimide is used for high reliability printed circuit boards in extreme temperature environments, such as aerospace and defense applications. It is compatible with multilayer PCB fabrication and can be used for flexible or rigid-flex boards.
  • Rogers Materials: Specialized high-frequency materials designed for applications requiring excellent signal integrity, such as aerospace and telecommunications. Rogers materials offer low dielectric loss, controlled impedance, and high thermal conductivity. They are often used in multilayer PCB fabrication for high-speed, high-frequency high reliability board.
  • High-Grade Copper Foils: Thick copper foils (1oz or more) are used for high reliability circuit boards to improve current-carrying capacity, thermal conductivity, and mechanical strength. Copper foils with high purity (99.9% or higher) reduce resistance and minimize signal loss. For multilayer PCB fabrication, copper foils are bonded to substrate layers to form conductive traces.
  • Lead-Free Solder: Compliant with RoHS standards, lead-free solder (such as SAC305) is used for high reliability PCB to ensure environmental safety and long-term reliability. Lead-free solder offers better thermal fatigue resistance than traditional lead-based solder, making it suitable for applications with frequent temperature cycles. It is essential for multilayer PCB fabrication where solder joints must withstand harsh conditions.
  • Underfill Materials: Used for BGA and CSP components, underfill materials fill the gap between the component and the PCB, improving mechanical strength and thermal conductivity. Underfill materials protect solder joints from vibration and thermal stress, reducing the risk of failure. They are commonly used in high reliability printed circuit boards for aerospace and medical applications.

What Special Requirements Are There for High Reliability PCB for Aerospace Applications?

Aerospace applications present unique challenges for high reliability PCB, including extreme temperatures, radiation, and strict weight constraints. These boards must meet rigorous standards to ensure safety and performance in space and aviation environments. Here are the special requirements for aerospace-grade high reliability PCB.

  • Extreme Temperature Resistance: Aerospace high reliability PCB must withstand temperatures ranging from -55°C to 125°C (or higher) during operation. Materials such as polyimide or Rogers are used to ensure thermal stability, and multilayer PCB fabrication is optimized to prevent layer separation at extreme temperatures. Thermal cycling testing is required to verify performance under temperature extremes.
  • Radiation Hardening: Boards used in space applications must be radiation-hardened to resist the effects of ionizing radiation, which can damage components and cause board failure. Radiation-hardened components and materials are used, and multilayer PCB fabrication processes are designed to minimize radiation-induced defects.
  • Lightweight and Compact Design: Aerospace systems have strict weight and space constraints, so high reliability PCB must be lightweight and compact. Multilayer PCB fabrication allows for high component density, reducing board size and weight while maintaining reliability. Lightweight materials such as polyimide are preferred to minimize overall system weight.
  • Mechanical Vibration and Shock Resistance: Aerospace high reliability board must withstand intense vibration and shock during launch and operation. Design features such as thick copper layers, reinforced mounting points, and proper component placement are used to enhance mechanical robustness. Multilayer PCB fabrication with strong lamination bonds ensures the board can withstand these stresses.
  • Low Outgassing: Materials used in aerospace high reliability PCB must have low outgassing to prevent contamination of sensitive equipment (such as optical systems) in the vacuum of space. Materials are tested for outgassing according to NASA standards, and only low-outgassing materials are used in multilayer PCB fabrication.
  • Traceability and Compliance: Aerospace high reliability printed circuit boards must comply with strict industry standards, including MIL-PRF-55110 and AS9100. Full traceability of materials, manufacturing processes, and testing results is required to ensure quality and accountability. Multilayer PCB fabrication processes are documented in detail to meet these requirements.

How to Design High Reliability Multilayer PCB to Withstand Harsh Environments?

Multilayer PCB are often the preferred choice for high reliability applications due to their compact design and enhanced performance. Designing these boards to withstand harsh environments requires specific optimizations to their layer structure, materials, and component placement. Below are the key steps to achieve this.

  • Layer Stackup Optimization: Design the layer stackup to maximize thermal management, signal integrity, and mechanical robustness. Use dedicated power and ground layers to reduce noise and improve signal quality. Multilayer PCB fabrication allows for precise layer placement, with signal layers between power and ground layers to minimize interference. Include thermal layers to distribute heat evenly across the board.
  • Use High-Quality Lamination Materials: Select lamination materials with high Tg and excellent adhesion to ensure layer bonding in harsh environments. For multilayer PCB fabrication,use lamination processes with controlled temperature and pressure to ensure no delamination. Materials such as high-Tg FR-4 or polyimide are ideal for harsh environment applications.
  • Thermal Via Placement: Incorporate thermal vias to transfer heat from the surface layer to internal thermal layers or heat sinks. Thermal vias should be placed near high-heat components and spaced evenly to maximize heat dissipation. Multilayer PCB fabrication allows for thermal vias that pass through multiple layers, improving thermal conductivity.
  • Reinforce Mechanical Structure: Use thicker core materials and copper layers to enhance mechanical strength. Avoid large unsupported areas on the board, as they are prone to bending and warping. Multilayer PCB fabrication can include stiffener layers to improve mechanical robustness, making the board resistant to vibration and shock.
  • Seal and Coat the Board: Apply conformal coating to protect the board from moisture, dust, and chemical exposure. Conformal coatings such as urethane or silicone create a barrier that prevents corrosion and component damage. For multilayer PCB fabrication, conformal coating is applied after assembly to ensure all components and traces are protected.
  • Test for Harsh Environment Performance: Subject the multilayer PCB to environmental testing, including thermal cycling, humidity testing, salt spray testing, and vibration testing. Testing simulates real-world harsh conditions and identifies potential points of failure. Multilayer PCB fabrication processes are adjusted based on testing results to improve reliability.
  • Optimize Component Placement: Place components to minimize stress on the board and ensure even heat distribution. Heavy components should be mounted securely, and heat-sensitive components should be placed away from high-heat areas. Multilayer PCB fabrication allows for compact component placement, reducing the risk of mechanical stress and improving thermal management.
High Reliability circuit board, https://www.bestpcbs.com/blog/2026/05/high-reliability-circuit-board/

What Testing Methods Are Used to Verify the Reliability of High Reliability Boards?

Verifying the reliability of high reliability boards requires comprehensive testing to simulate real-world conditions and identify potential defects. These tests ensure the board can withstand thermal stress, vibration, moisture, and other harsh factors. Here are the key testing methods used to validate reliability.

  • Thermal Cycling Testing: Exposes the high reliability board to extreme temperature cycles (e.g., -55°C to 125°C) to test thermal fatigue resistance. This test simulates real-world temperature changes and identifies issues such as solder joint cracking, layer delamination, or component failure. Thermal cycling is critical for multilayer PCB fabrication, as it verifies the board’s ability to withstand temperature-induced stress.
  • Vibration Testing: Applies controlled vibration to the board to simulate the mechanical stress of applications such as aerospace, automotive, or industrial equipment. Vibration testing identifies loose components, solder joint failures, or board warping. For high reliability PCB, vibration testing is performed at various frequencies and amplitudes to ensure robustness.
  • Humidity Testing: Exposes the board to high humidity (e.g., 85% RH at 85°C) to test resistance to moisture. Moisture can cause corrosion, short circuits, or layer delamination, so humidity testing is essential for high reliability printed circuit boards used in humid environments. Testing duration varies based on application requirements.
  • X-Ray Inspection: Uses X-ray technology to inspect internal components, solder joints, and layer alignment. X-ray inspection is critical for multilayer PCB fabrication, as it detects hidden defects such as voids in solder joints, misaligned layers, or internal shorts that cannot be seen with visual inspection.
  • Continuity and Insulation Resistance Testing: Verifies that traces are continuous and that there is no unintended electrical connection between traces (short circuits). Insulation resistance testing ensures that the board’s insulation materials prevent current leakage. These tests are performed on every high reliability PCB to ensure electrical performance.
  • Mechanical Shock Testing: Applies sudden mechanical shock to the board to simulate impact events (e.g., drops, collisions). Shock testing identifies structural weaknesses, such as cracked traces or loose components, that could lead to failure. High reliability board used in portable or high-impact applications require rigorous shock testing.
  • Accelerated Life Testing (ALT): Subjects the board to accelerated environmental conditions (e.g., high temperature, high humidity) to simulate long-term use in a short period. ALT predicts the board’s service life and identifies potential failure modes early. This test is essential for high reliability printed circuit boards used in critical applications.

What Common Issues Arise in High Reliability Circuit Board Assembly and How to Solve Them?

Even with strict quality control, assembly of high reliability circuit boards can encounter common issues that threaten performance. Identifying these problems early and implementing effective solutions is critical to maintaining the board’s reliability. Below are the most frequent issues and their resolutions.

  • Solder Joint Voiding: Voiding in solder joints reduces mechanical strength and thermal conductivity, leading to premature failure. To solve this, use high-quality lead-free solder paste, optimize reflow profiles to ensure complete solder melting, and inspect solder joints with X-ray technology. For multilayer PCB fabrication, ensure proper stencil design to control solder paste volume.
  • Layer Delamination: Delamination occurs when layers of the PCB separate due to poor lamination, moisture, or thermal stress. To solve this, use high-quality lamination materials with high Tg, control humidity during assembly, and optimize thermal cycling processes. Multilayer PCB fabrication should use controlled temperature and pressure during lamination to ensure strong layer adhesion.
  • Component Misalignment: Misaligned components can cause short circuits, poor signal integrity, or mechanical stress. To solve this, use automated pick-and-place machines with high accuracy, inspect component placement with AOI systems, and ensure stencil alignment is precise. For high reliability PCB, component placement should be verified before reflow soldering.
  • Trace Damage: Trace damage (e.g., scratches, breaks) can cause open circuits or signal degradation. To solve this, handle boards carefully during assembly, use protective coatings to prevent scratches, and inspect traces with AOI or visual inspection. Multilayer PCB fabrication should use high-quality copper foils to reduce trace brittleness.
  • Moisture Contamination: Moisture can seep into the PCB during assembly, causing corrosion or delamination. To solve this, bake boards before assembly to remove moisture, store components in dry environments, and apply conformal coating after assembly. High reliability printed circuit boards should be sealed to prevent moisture ingress.
  • Thermal Overheating: Overheating can damage components and reduce board reliability. To solve this, optimize thermal management design (e.g., thermal vias, heat sinks), select components with high temperature ratings, and ensure proper airflow around the board. Multilayer PCB fabrication can include dedicated thermal layers to distribute heat evenly.

How to Choose the Right Manufacturer for Printed Circuit Board Assembly High Reliability?

Selecting the right manufacturer is a critical step in ensuring the quality and reliability of your high reliability PCB. Not all manufacturers have the expertise or capabilities to meet the strict standards required for these specialized boards. Here’s what to look for when choosing a manufacturer.

  • Verify Industry Certifications: Choose a manufacturer with certifications such as AS9100 (aerospace), ISO 13485 (medical), or IPC-6012 (PCB qualification). Certifications ensure the manufacturer follows strict quality control processes for high reliability PCB. Verify that the manufacturer has experience with multilayer PCB fabrication for high reliability applications.
  • Assess Manufacturing Capabilities: Ensure the manufacturer has the equipment and expertise for high precision manufacturing, including multilayer PCB fabrication, automated assembly, and advanced testing. Check if they can handle specialized materials (e.g., polyimide, Rogers) and strict tolerances required for high reliability board.
  • Review Quality Control Processes: Ask about the manufacturer’s quality control processes, including material inspection, in-process testing, and final inspection. A reliable manufacturer will have 100% inspection for high reliability printed circuit boards and detailed documentation of all processes. Verify that they use AOI, X-ray, and environmental testing to ensure quality.
  • Evaluate Experience in Critical Applications: Choose a manufacturer with experience in your industry (e.g., aerospace, medical) to ensure they understand the unique requirements of high reliability PCB. Ask for case studies or references from clients in similar applications, especially those involving multilayer PCB fabrication.
  • Check Traceability and Documentation: Ensure the manufacturer provides full traceability of materials, components, and manufacturing processes. Detailed documentation is essential for compliance with industry standards and for root cause analysis if defects occur. This includes records of multilayer PCB fabrication, assembly, and testing.
  • Assess Customer Support and Communication: A reliable manufacturer will provide clear communication throughout the manufacturing process and offer technical support for design optimization. They should be able to answer questions about multilayer PCB fabrication, material selection, and testing, and provide timely updates on order status.
  • Compare Lead Times and Pricing: While quality is the top priority for high reliability board, compare lead times and pricing to ensure they align with your project timeline and budget. Avoid manufacturers with unusually low pricing, as this may indicate lower quality materials or processes. Ensure the manufacturer can meet your deadlines without compromising quality.

What Industry Standards Must High Reliability Circuit Boards Comply With?

High reliability circuit boards must adhere to strict industry standards to ensure consistency, safety, and performance. These standards govern materials, manufacturing, testing, and assembly, varying by application. Below are the key standards that apply to high reliability PCB.

  • IPC-6012: A standard for the qualification and performance of rigid printed boards, including high reliability PCB.It specifies requirements for material quality, manufacturing processes, and testing. IPC-6012 is critical for multilayer PCB fabrication, as it sets standards for layer alignment, trace quality, and lamination.
  • IPC-A-610: A standard for the acceptability of electronic assemblies. It provides guidelines for solder joint quality, component placement, and board cleanliness. High reliability printed circuit boards must comply with IPC-A-610 Class 3 (the highest class) for critical applications.
  • MIL-PRF-55110: A military standard for rigid printed circuit boards used in aerospace and defense applications.It specifies strict requirements for materials, manufacturing, and testing, including thermal stability, mechanical robustness, and radiation resistance. Compliance with MIL-PRF-55110 is essential for high reliability board in military systems.
  • AS9100: A quality management system standard for the aerospace industry. Manufacturers of high reliability PCB for aerospace applications must be AS9100 certified to ensure compliance with strict quality and safety requirements. AS9100 covers all aspects of manufacturing, including multilayer PCB fabrication and assembly.
  • ISO 13485: A standard for quality management systems in the medical device industry. High reliability printed circuit boards used in medical devices must comply with ISO 13485 to ensure safety and effectiveness. This standard includes requirements for traceability, documentation, and risk management.
  • RoHS: A European Union standard that restricts the use of hazardous substances (e.g., lead, cadmium) in electronic products. High reliability PCB must comply with RoHS to ensure environmental safety and global market access. This includes using lead-free solder and RoHS-compliant materials in multilayer PCB fabrication.
  • UL 94: A standard for flammability of plastic materials used in electronic devices. High reliability board must comply with UL 94 to ensure they do not catch fire or spread flame in the event of a short circuit. This is critical for applications such as automotive and industrial equipment.

How Does High Reliability PCB Design Impact the Lifespan of Electronic Devices?

The design of a high reliability PCB has a direct and significant impact on the overall lifespan of the electronic device it powers. From thermal management to component selection, every design choice influences how long the device can operate reliably. Here’s how design decisions affect device lifespan.

  • Thermal Management Design: Proper thermal management in high reliability PCB design prevents overheating, which is a leading cause of component failure. By incorporating heat sinks, thermal vias, and dedicated thermal layers through multilayer PCB fabrication, the board dissipates heat efficiently, extending the lifespan of components and the overall device.
  • Mechanical Robustness: High reliability PCB designed for mechanical robustness (e.g., thick copper layers, reinforced mounting points) can withstand vibration, shock, and physical stress. This reduces the risk of component damage or board failure, extending the device’s lifespan. Multilayer PCB fabrication enhances mechanical robustness by ensuring strong layer adhesion and structural integrity.
  • Component Selection and Placement: Selecting high-reliability components and placing them strategically reduces the risk of component failure. Components placed away from heat sources and vibration points last longer, while redundant components ensure the device continues functioning if one component fails. This directly extends the device’s lifespan.
  • Signal Integrity Optimization: Poor signal integrity can cause errors, component damage, or system failure. High reliability PCB design with controlled impedance, minimal crosstalk, and proper trace routing ensures consistent signal performance. Multilayer PCB fabrication allows for signal layer isolation, improving signal integrity and reducing component wear.
  • Material Selection: Using high-quality materials (e.g., high-Tg FR-4, polyimide) in high reliability printed circuit boards ensures the board resists degradation from temperature, moisture, and chemical exposure.These materials have a longer service life, directly extending the lifespan of the electronic device. Multilayer PCB fabrication with high-quality materials enhances durability.
  • Testing and Quality Control: High reliability PCB design includes rigorous testing to identify and eliminate potential defects before the board is integrated into the device. This reduces the risk of premature failure and ensures the board operates reliably for its entire service life, extending the device’s lifespan.
  • Environmental Protection: Design features such as conformal coating and moisture sealing protect the high reliability board from harsh environmental conditions. This prevents corrosion, short circuits, and component damage, extending the board’s service life and the overall device lifespan. Multilayer PCB fabrication with sealed layers further enhances environmental protection.
High Reliability Circuit Board, https://www.bestpcbs.com/blog/2026/05/high-reliability-circuit-board/

FAQ About High Reliability Circuit Board

Q1: What is the difference between high reliability circuit board and standard PCB?

A1: High reliability circuit board are designed for durability in harsh or critical environments, using high-grade materials, strict manufacturing tolerances, and comprehensive testing. Standard PCB use lower-quality materials, wider tolerances, and basic testing, making them suitable for non-critical applications. Multilayer PCB fabrication for high reliability also involves more precise processes than standard multilayer boards.

Q2: What materials are best for high reliability printed circuit boards?

A2: The best materials for high reliability printed circuit boards include high-Tg FR-4 (for general applications), polyimide (for extreme temperatures), and Rogers materials (for high-frequency applications). High-grade copper foils, lead-free solder, and underfill materials also enhance reliability, especially in multilayer PCB fabrication.

Q3: How does multilayer PCB fabrication impact high reliability?

A3: Multilayer PCB fabrication enhances high reliability by allowing for greater component density, improved signal integrity, better thermal management, and increased mechanical robustness. Precise lamination processes in multilayer PCB fabrication ensure layer adhesion, while dedicated thermal and signal layers optimize performance in harsh environments.

Q4: What testing is required for high reliability board?

A4: High reliability board require comprehensive testing, including thermal cycling, vibration testing, humidity testing, X-ray inspection, continuity testing, mechanical shock testing, and accelerated life testing. These tests verify the board’s ability to withstand harsh conditions and ensure long-term reliability.

Q5: What industry standards apply to high reliability PCB?

A5: Key industry standards for high reliability PCB include IPC-6012 (PCB qualification), IPC-A-610 (assembly acceptability), MIL-PRF-55110 (military), AS9100 (aerospace), ISO 13485 (medical), RoHS (environmental), and UL 94 (flammability). Compliance with these standards ensures quality and reliability.

Q6: How to choose a manufacturer for high reliability PCB assembly?

A6: Choose a manufacturer with relevant certifications (AS9100, ISO 13485), experience in high reliability applications, advanced manufacturing capabilities (including multilayer PCB fabrication), strict quality control processes, full traceability, and strong customer support. Evaluate their testing capabilities and references from similar clients.
You may also like

What are Electron Devices and Circuits? PCB Design Basics

May 8th, 2026

What Are Electron Devices and Circuits?

Electron devices and circuits are the foundation of electronic products. An electron device is a component that controls current, voltage, or signal behavior. A circuit is the connected network that allows these devices to perform a useful function, such as switching, amplification, filtering, rectification, sensing, timing, or power conversion.

Common electron devices include diodes, transistors, MOSFETs, integrated circuits, sensors, voltage regulators, and operational amplifiers. These parts do not work alone in a finished product. They are connected through copper traces, vias, pads, and planes on a printed circuit board.

In simple terms, a device is the part. A circuit is the working system built with parts. A PCB is the physical platform that makes the circuit reliable, manufacturable, and suitable for real-world use.

What Are Electron Devices and Circuits?

Why Are Electron Devices and Circuits Important in Modern Electronics?

Electron devices and circuits are important because almost every electronic product depends on them to process signals, control power, and respond to the outside world. Without them, a PCB would only be a passive copper structure. The devices give the board intelligence, control, and function.

Modern electronics use circuits in many forms, a medical monitor uses sensor circuits and signal conditioning. An electric vehicle uses power control circuits and protection circuits. A telecom product uses RF circuits and high-speed digital paths. Industrial equipment uses control circuits, relay drivers, motor drivers, and power supply sections.

What Is the Difference Between Electronic Devices and Electronic Circuits?

Electronic devices are individual components. Electronic circuits are functional networks made by connecting those components. The difference is similar to the relationship between bricks and a building. A component may have a clear function, but the circuit decides how that function is used.

ItemMeaningExamplePCB Concern
Electronic deviceA single component that controls or responds to electricityDiode, MOSFET, IC, sensorFootprint, polarity, package, rating
Electronic circuitA connected group of devices and passive partsAmplifier, filter, power supplyRouting, grounding, noise, heat
PCB layoutThe physical copper and component arrangementTraces, vias, planes, padsManufacturability and signal quality
PCBAA finished assembled circuit boardPCB with components solderedTesting, inspection, reliability
Final systemThe board inside a working productMedical device, IoT module, inverterCompliance, durability, user safety

A circuit may look correct on a schematic but still perform poorly on the actual PCB. Long current loops, weak grounding, wrong component placement, thin copper paths, or poor thermal design can change the behavior of the circuit. This is why circuit design and PCB layout should not be treated as separate jobs.

What Are the Main Types of Electron Devices?

The main types of electron devices include diodes, bipolar junction transistors, MOSFETs, IGBTs, operational amplifiers, sensors, voltage regulators, and integrated circuits. Each device has a specific role in controlling current, voltage, timing, power, or signal behavior. Below are the most common electronic components in the market and their basic functions:

What Are the Main Types of Electron Devices?

For PCB projects, the selected device package is as important as the device itself. A MOSFET in a small SOT-23 package cannot dissipate the same heat as a larger DPAK or PowerPAK package. A high-speed IC may require controlled impedance routing. A sensor may need clean analog grounding and physical isolation from heat sources.

How Do Diodes Work in Electronic Circuits?

Diodes mainly control current direction. They are often used to convert AC to DC, protect circuits from reverse polarity, clamp voltage spikes, and provide flyback protection for inductive loads such as relays, coils, and motors.

A standard silicon diode often has a forward voltage drop of about 0.6–0.8 V under typical operating conditions. A Schottky diode usually has a lower forward voltage, often around 0.2–0.5 V, making it useful in low-voltage and power-sensitive circuits.

Diode TypeTypical Forward VoltageCommon UsePCB Design Focus
Silicon diode0.6–0.8 VRectification, protectionPolarity, current rating
Schottky diode0.2–0.5 VLow-loss power pathsLeakage current, heat
Zener diodeDepends on Zener voltageVoltage clamp/referencePower dissipation
TVS diodeApplication-specificESD/surge protectionPlace close to connector
LED1.8–3.3 V typicalIndication, lightingCurrent limit and heat

How Do Transistors and MOSFETs Control Current?

Transistors and MOSFETs control current by using a smaller signal to manage a larger load. A BJT is commonly driven by base current, while a MOSFET is driven by gate voltage. Both can switch loads, but MOSFETs are often preferred for efficient power switching.

How Do Transistors and MOSFETs Control Current?

A BJT may be useful for small-signal amplification and low-current switching. A MOSFET is widely used in DC-DC converters, motor drivers, LED drivers, battery protection circuits, and power distribution boards. The choice depends on voltage, current, switching speed, drive voltage, heat, package size, and cost.

What Are the Most Common Electronic Circuit Types?

The most common electronic circuit types include rectifier circuits, amplifier circuits, filter circuits, oscillator circuits, switching circuits, voltage regulator circuits, sensor interface circuits, logic circuits, and power supply circuits. Each one solves a specific electrical task.

What Are the Most Common Electronic Circuit Types?

A practical PCB often contains several circuit types on the same board. For example, an industrial control board may include power input protection, DC-DC conversion, MCU logic, sensor input, relay output, and communication ports. The design challenge is to make these sections work together without noise, overheating, or assembly issues.

How Do Electron Devices and Circuits Become a PCB?

Electron devices and circuits become a PCB through a structured process: schematic design, BOM preparation, PCB layout, design review, Gerber output, fabrication, component sourcing, SMT assembly, inspection, testing, and final shipment. The schematic defines the electrical logic. The PCB layout turns that logic into a manufacturable board.

The process usually starts with circuit requirements, such as: What voltage does the board need? What current will it carry? What signals are sensitive? What connector, enclosure, and environmental requirements must be considered? These answers guide the schematic and layout.

A typical flow looks like this:

How Do Electron Devices and Circuits Become a PCB?

1. Define product function and electrical requirements.

2. Select suitable components and packages.

3. Build the schematic and check circuit behavior.

4. Create the PCB stack-up and layout rules.

5. Place components according to function, heat, and signal flow.

6. Route power, ground, analog, digital, and high-speed signals.

7. Add test points, markings, fiducials, and assembly details.

8. Run DRC, ERC, DFM, and DFT checks.

9. Fabricate the bare PCB.

10. Source components and prepare SMT programming.

11. Assemble the board through SMT, DIP, or mixed assembly.

12. Inspect and test the PCBA before delivery.

The earlier manufacturability is considered, the smoother the project becomes. A schematic can be electrically correct, but if the selected package is unavailable, the footprint is wrong, or the thermal path is weak, the final build may face delay or rework.

What PCB Design Rules Matter for Electronic Devices and Circuits?

The PCB design rules that matter most include trace width, spacing, grounding, return path, decoupling capacitor placement, thermal relief, creepage, clearance, impedance control, component orientation, and test point access. These rules help the circuit perform as intended after manufacturing.

Design ItemWhy It MattersPractical Rule of Thumb
Trace widthControls current capacity and heatingWider copper for power paths
SpacingReduces short risk and voltage breakdownIncrease spacing for higher voltage
Ground planeProvides stable reference and return pathUse continuous ground where possible
Decoupling capacitorStabilizes IC power pinsPlace close to power pins
Thermal viaMoves heat to other copper layersUse near power IC pads
Test pointSupports inspection and troubleshootingAdd to power rails and signals
Component orientationReduces assembly mistakesKeep polarity markings clear
Controlled impedanceMaintains high-speed signal qualityDefine stack-up early

One useful principle is to place parts according to current and signal flow. Power input should connect logically to protection, filtering, conversion, and load sections. Sensitive analog circuits should stay away from noisy switching nodes and high-speed signals should avoid unnecessary stubs and discontinuities.

What Causes Electron Devices and Circuits to Fail?

Electron devices and circuits usually fail because of overstress, poor layout, incorrect component selection, weak soldering, thermal buildup, electrical noise, or manufacturing defects. Many failures can be reduced through early design review and proper test planning.

Common causes include:

Failure CauseWhat HappensHow to Reduce the Risk
OvercurrentDevice or trace overheatsUse current rating, fuse, wider copper
OvervoltageIC or diode damageAdd TVS, Zener, clamp, margin
ESDSudden device failureUse ESD protection near connectors
Thermal stressDrift, aging, solder fatigueAdd copper area, vias, airflow path
Wrong footprintAssembly mismatchCheck datasheet and land pattern
Poor solder jointIntermittent functionUse AOI, X-ray, proper stencil design
Noise couplingSignal error or resetSeparate noisy and sensitive circuits
Weak test coverageHidden defectsAdd ICT/flying probe/function test

How Should Beginners Learn Electron Devices and Circuits?

Beginners should learn electron devices and circuits in a step-by-step order: basic electrical laws, passive components, diodes, transistors, MOSFETs, op-amps, power circuits, digital logic, PCB layout, and testing. This path makes the subject easier because each new topic builds on the previous one.

A good learning route starts with voltage, current, resistance, and power. Then it moves into resistors, capacitors, and inductors. After that, diodes and transistors become easier to understand. Once active devices are clear, amplifiers, filters, regulators, and switching circuits become more practical.

A beginner-friendly study path may look like this:

Learning StageWhat to LearnPractical Exercise
Stage 1Voltage, current, resistance, powerCalculate LED current resistor
Stage 2Resistors, capacitors, inductorsBuild RC filter
Stage 3Diodes and rectifiersBuild bridge rectifier
Stage 4BJT and MOSFET switchingDrive LED, relay, or motor
Stage 5Op-amp circuitsBuild non-inverting amplifier
Stage 6Power supply circuitsTest regulator output and ripple
Stage 7PCB layout basicsConvert schematic to PCB
Stage 8Testing and debuggingMeasure voltage, current, waveform

How Are Electron Devices and Circuits Used in Real PCB Applications?

Electron devices and circuits are used in almost every PCB application, including medical electronics, automotive systems, telecom equipment, industrial control, robotics, power electronics, smart sensors, LED lighting, consumer devices, and IoT products. Here we listing some applications of electron devices and their typical circuit needs:

ApplicationTypical Circuit Needs
Medical electronicsSensor input, signal conditioning, power control
Industrial controlRelay output, PLC interface, motor control
Automotive electronicsPower switching, communication, protection
Telecom equipmentRF, high-speed digital, power supply
IoT devicesMCU, wireless module, battery management
LED lightingConstant-current driver, thermal path
RoboticsMotor driver, sensor fusion, control logic

How Can PCB Layout Improve Circuit Performance?

PCB layout can improve circuit performance by reducing noise, controlling heat, shortening current loops, protecting sensitive signals, and making the board easier to assemble and test. Layout is not only about connecting pins, it directly affects electrical behavior.

Several layout habits are helpful:

  • Place decoupling capacitors close to IC power pins.
  • Keep high-current paths short and wide.
  • Avoid routing sensitive analog signals near switching nodes.
  • Use a continuous ground plane where possible.
  • Place protection devices close to external connectors.
  • Add enough test points for production and troubleshooting.
  • Review footprints before releasing Gerber files.
  • Separate hot components from temperature-sensitive parts.

A clean layout can make a modest circuit perform very well. A poor layout can make a good schematic unstable.

How Can EBest Support PCB Projects for Electron Devices and Circuits?

EBest supports PCB projects by helping customers move from schematic and BOM to PCB fabrication, component sourcing, PCBA assembly, testing, and delivery. This is useful for projects that involve power circuits, sensor circuits, control boards, communication modules, medical electronics, industrial electronics, automotive electronics, and telecom hardware.

EBest Circuit provides:

  • PCB fabrication for prototypes and production
  • PCBA assembly for SMT, DIP, and mixed-technology boards
  • Component sourcing and BOM optimization
  • DFM review before manufacturing
  • AOI, X-ray, ICT, flying probe, and functional testing options
  • Engineering communication for complex PCB and PCBA projects
  • Support for industrial, medical, automotive, telecom, IoT, and power electronics applications

A circuit becomes valuable only when it can be built reliably. By combining PCB manufacturing, assembly, sourcing, and testing, EBest helps customers reduce communication gaps and move faster from design files to finished boards.

For project review, customers can send schematic, BOM, Gerber files, or assembly drawings to sales@bestpcbs.com.

FAQs About Electron Devices and Circuits

1. What are electron devices and circuits?

Electron devices and circuits are the components and connections that allow electronic systems to control current, voltage, signals, and power. Devices include diodes, transistors, MOSFETs, ICs, sensors, and op-amps. Circuits connect these parts to perform functions such as switching, amplification, filtering, protection, sensing, and power conversion.

2. What is the difference between electrical circuits and electronic circuits?

An electron device is an individual component (like a transistor or diode) that controls the flow of electrons to perform a specific function. An electronic circuit is a complete path or network of these devices connected together with passive components (resistors, capacitors) to process signals or manage power.

3. Why is silicon the most commonly used material in electron devices?

Silicon is preferred because it is abundant, relatively inexpensive, and has excellent thermal stability. Most importantly, it naturally forms a high-quality silicon dioxide layer, which is essential for manufacturing MOSFETs (Metal-Oxide-Semiconductor Field-Effect Transistors), the building blocks of modern chips.

4. How does a P-N junction diode work?

A P-N junction diode is formed by joining p-type (positive) and n-type (negative) semiconductor materials. It acts as a one-way valve for electricity: in “forward bias,” it allows current to flow easily, whereas in “reverse bias,” it blocks current by creating a depletion region that prevents electrons from crossing.

5. What is the difference between analog and digital circuits?

Analog circuits process continuous signals that vary in voltage or current (like sound waves). Digital circuits process discrete signals, representing data as “high” or “low” voltages (1s and 0s). While analog is used for real-world sensing, digital is favored for processing and data storage due to its resistance to noise.

You may also like

What is Burn in Board? Burn in Board vs Load Board

May 7th, 2026

How do electronic manufacturers ensure their products avoid early failures and maintain long-term reliability? The solution lies in a critical testing component known as a burn in board. It is a tool that separates high-quality electronic components from those prone to premature breakdown.

This article breaks down everything about burn in boards, from their core definition to practical applications, design principles, cost factors, and key differences from load boards. Whether working with consumer electronics, industrial equipment, or automotive components, the insights here help make informed decisions about testing processes, material selection, and manufacturer partnerships.

Burn in Board, https://www.bestpcbs.com/blog/2026/05/burn-in-board/

What is a Burn in Board (BIB)?

A Burn in Board (BIB), also called an aging board, is a specialized printed circuit board (PCB) built to facilitate burn in testing a reliability screening process for electronic components. Its main function is to expose components to extreme environmental conditions, such as high temperatures, elevated voltage, and continuous operational load, to speed up the detection of potential defects and early-stage failures.

Unlike standard PCBs, burn in boards are engineered to handle harsh testing environments without losing performance. They come with specialized connectors, heat-dissipating structures, and precise wiring to ensure uniform stress application across all tested components. This controlled stress testing simulates years of normal use in just hours or days, letting manufacturers identify and discard faulty components before they reach end users.

Burn in boards are customized to match the specific form factor and electrical requirements of the components being tested. This customization ensures each component receives the exact stress levels needed to uncover hidden flaws, such as poor solder joints, weak semiconductor bonds, or material inconsistencies that could cause failures after deployment.

Why Do People Use Burn in Boards?

Using burn in boards is a strategic investment in product reliability, addressing common challenges like high return rates, costly recalls, and damaged brand reputation. The following points outline the main reasons manufacturers depend on these specialized boards for electronic component testing.

  • Eliminate Early Failures Most electronic component failures happen within the first few hundred hours of use, a phenomenon called infant mortality. Burn in testing with a burn in board accelerates this phase, weeding out defective components before they are integrated into final products. This cuts down on post-purchase failures and the related costs of repairs, replacements, and customer support.
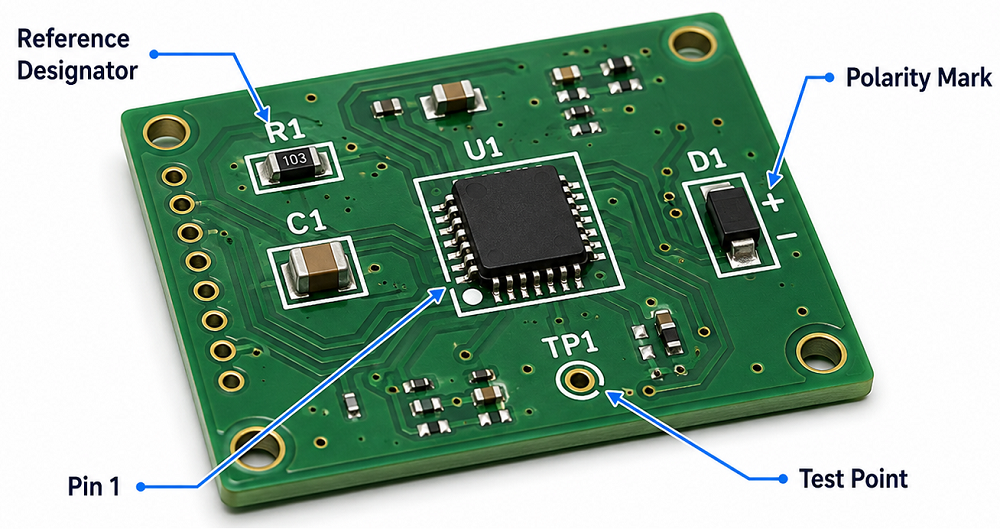
  • Ensure Long-Term Reliability Components that pass burn in testing are more likely to maintain performance over their intended lifespan. This is critical for industries like automotive, aerospace, and medical devices, where component failure can lead to safety hazards, regulatory non-compliance, or catastrophic system breakdowns.
  • Reduce Warranty and Recall Costs Recalls and warranty claims can drain resources and harm brand trust. By screening components with a burn in board, manufacturers lower the risk of shipping faulty products, reducing warranty expenses and avoiding the negative impact of public recalls.
  • Comply with Industry Standards Many industries have strict reliability requirements that require burn in testing. For example, automotive components must meet AEC-Q100 standards, while medical devices need compliance with ISO 13485. Burn in boards enable manufacturers to meet these standards and gain certification for their products.
  • Optimize Production Efficiency Identifying defects early in the production process reduces waste and rework. Burn in testing allows manufacturers to address issues at the component level, rather than after assembly, saving time and resources that would otherwise go to disassembling and repairing faulty products.
Burn in Board, https://www.bestpcbs.com/blog/2026/05/burn-in-board/

What is the Difference Between Burn in Board and Load Board?

Burn in boards and load boards are both used in electronic testing, but they serve distinct purposes and operate under different principles. The table below clearly outlines their key differences, helping avoid common confusion between these two critical testing tools.

Comparison FactorBurn in BoardLoad Board
Primary PurposeScreen for early failures and ensure long-term reliability by subjecting components to extreme stress (high temperature, voltage).Test the functional performance of components under normal or specified load conditions to verify operational correctness.
Testing EnvironmentOperates in harsh environments, often paired with burn in chambers to maintain high temperatures (70°C+).Operates in standard laboratory conditions, focusing on normal operating temperatures and voltages.
Component Stress LevelApplies elevated stress (above normal operating limits) to accelerate failure detection.Applies nominal or specified load levels to simulate real-world operational conditions.
Design FocusBuilt for durability, heat resistance, and uniform stress distribution across components.Built for precision, signal integrity, and accurate measurement of component performance.
Typical ApplicationsConsumer electronics, automotive components, industrial equipment, medical devices.Semiconductor testing, PCB functional testing, high-volume production line testing.
Testing DurationLonger duration (hours to days) to ensure thorough stress exposure.Shorter duration (seconds to minutes) for quick functional verification.

What Are the Design Principles for a High-Quality Burn in Board?

Designing a high-quality burn in board requires careful consideration of testing requirements, environmental conditions, and component compatibility. The following principles ensure the board delivers consistent, reliable results while withstanding the rigors of burn in testing.

  • Thermal Management: Burn in testing generates significant heat, so effective thermal management is essential. The board should feature heat-dissipating structures, such as thick copper traces, thermal vias, or metal substrates, to prevent overheating and ensure uniform temperature distribution across all tested components. This avoids false failures caused by localized hotspots.
  • Electrical Compatibility: The board must be electrically compatible with the components being tested, including matching voltage, current, and signal requirements. Proper impedance matching and isolation between circuits prevent cross-talk and ensure accurate stress application.
  • Durability and Longevity: Burn in boards are subjected to repeated high-stress testing cycles, so they must be built with durable materials and robust construction. This includes using high-temperature resistant substrates, corrosion-resistant connectors, and reinforced solder joints to withstand extended use.
  • Uniform Stress Application: Every component on the board must receive the same level of stress to ensure consistent testing results. This requires precise wiring, balanced load distribution, and careful component placement to avoid variations in voltage or temperature across the board.
  • Customization Flexibility: Different components require different testing parameters, so the board should be designed with customization in mind. Modular designs or interchangeable components allow for easy adaptation to different component form factors and testing requirements, reducing the need for multiple dedicated boards.
  • Test Monitoring Capability: The board should include provisions for real-time monitoring of component performance during testing. This may include built-in sensors to track temperature, voltage, and current, allowing operators to identify failures as they occur and adjust testing parameters if needed.

Burn in Board Design Guidelines

Following specific design guidelines ensures that burn in boards meet performance standards and deliver reliable testing results. These guidelines address common design pitfalls and provide actionable steps to optimize board performance.

  • Select Appropriate Substrate Materials: Choose substrates with high glass transition temperatures (Tg) to withstand high testing temperatures. Common options include FR-4 TG170 or higher, ceramic, or metal-core substrates, depending on the testing environment and component requirements.
  • Optimize Trace Width and Spacing: Trace width should be sized to handle the maximum current during testing, preventing overheating and voltage drop. Trace spacing should be sufficient to avoid arcing or cross-talk, especially in high-voltage testing scenarios.
  • Use High-Quality Connectors: Select connectors rated for high temperatures and repeated use, such as press-fit or soldered connectors with gold plating to resist corrosion. Ensure connectors provide a secure, low-resistance connection to the tested components.
  • Incorporate Thermal Vias: Thermal vias transfer heat from the board surface to internal layers or heat sinks, improving heat dissipation. Place thermal vias near high-heat components and in dense component areas to prevent localized overheating.
  • Implement Proper Grounding: A robust grounding system reduces electromagnetic interference and ensures stable electrical performance. Use a solid ground plane and avoid ground loops, which can cause signal noise and inaccurate testing results.
  • Design for Easy Component Installation and Removal: The board should allow for quick and secure installation of components, with clear alignment guides and accessible connectors. This reduces testing downtime and minimizes the risk of component damage during handling.
  • Include Test Points for Troubleshooting: Add test points at key locations on the board to facilitate troubleshooting and performance verification. Test points allow operators to measure voltage, current, and temperature during testing, helping to identify issues with the board or tested components.
Burn in Board, https://www.bestpcbs.com/blog/2026/05/burn-in-board/

How is Burn in Testing Applied to Electronic Components Using a Burn in Board?

Burn in testing with a burn in board follows a structured process to ensure consistent, effective screening of electronic components. The steps below outline how to apply this testing method, from preparation to post-test analysis.

  • Prepare the Burn in Board: Verify that the board is properly configured for the specific components being tested. This includes checking component compatibility, ensuring all connectors are secure, and confirming that thermal management systems are functioning correctly. Calibrate any built-in sensors to ensure accurate temperature and voltage measurements.
  • Install Components: Mount the components to be tested onto the burn in board, following proper handling procedures to avoid damage. Ensure components are aligned correctly and securely fastened to prevent poor electrical connections or heat transfer issues.
  • Place the Board in a Burn in Chamber: Transfer the loaded burn in board to a burn in chamber, which controls temperature, humidity, and other environmental factors. Set the chamber to the required testing parameters, typically 70°C to 125°C, depending on the component type and industry standards.
  • Initiate the Burn in Test: Apply the specified voltage, current, and load to the board, starting the testing cycle. The duration of the test varies based on component type, ranging from 24 to 168 hours. Monitor the test in real time to track component performance and identify any immediate failures.
  • Monitor Test Parameters: Continuously check temperature, voltage, and current levels to ensure they remain within the specified range. Any deviations may indicate a problem with the board, chamber, or tested components, requiring immediate adjustment or termination of the test.
  • Terminate the Test and Inspect Components: Once the test cycle is complete, remove the burn in board from the chamber and allow it to cool to room temperature. Inspect each component for visible damage, such as bulging capacitors or burnt traces, and perform electrical tests to verify functionality.
  • Classify Components: Separate components into passing and failing categories based on test results. Passing components are cleared for further assembly, while failing components are discarded or sent for further analysis to identify the root cause of failure.

What Materials Are Commonly Used to Make Durable Burn in Boards?

The durability and performance of a burn in board depend heavily on the materials used in its construction. The following materials are commonly selected for their ability to withstand high temperatures, electrical stress, and repeated testing cycles.

  • FR-4 Glass Epoxy:The most common substrate material for burn in boards, FR-4 glass epoxy offers a good balance of cost, durability, and thermal resistance. FR-4 TG170 or higher grades are preferred for high-temperature testing, as they maintain structural integrity at temperatures up to 170°C. It is widely used for consumer electronics and industrial components testing.
  • Ceramic Substrates: Ceramic substrates, such as alumina (Al2O3) and aluminum nitride (AlN), provide excellent thermal conductivity and high-temperature resistance. They are ideal for testing high-power components, such as automotive semiconductors and industrial power modules, where heat dissipation is critical.
  • Metal-Core PCBs: Metal-core PCBs (MCPCBs) feature a metal base, typically aluminum or copper, which enhances heat dissipation. They are commonly used for burn in boards testing LED components, power amplifiers, and other high-heat devices. The metal core acts as a heat sink, reducing component temperature during testing.
  • High-Temperature Copper Foil: Thick copper foil (2 oz or higher) is used for traces and ground planes to improve current-carrying capacity and heat dissipation. Gold-plated copper foil is often used for connectors and test points to resist corrosion and ensure low-resistance connections.
  • Heat-Resistant Solder: Solder with a high melting point, such as lead-free solder (Sn-Ag-Cu) or high-temperature leaded solder (Sn-Pb), is used to assemble burn in boards. This prevents solder joints from melting during high-temperature testing, ensuring reliable electrical connections.
  • High-Temperature Connectors: Connectors made from heat-resistant materials, such as PEEK or LCP, are used to connect the burn in board to testing equipment. Gold-plated contacts provide corrosion resistance and ensure stable electrical performance over repeated testing cycles.

How Much Does a Burn in Board Cost?

The cost of a burn in board varies based on several factors, including design complexity, materials, customization requirements, and order quantity. Understanding these factors helps manufacturers budget effectively and select the most cost-efficient solution for their testing needs.

  • Design Complexity: Simple burn in boards for basic components (e.g., resistors, capacitors) cost less, typically ranging from $100 to $500 per unit. Complex boards for high-power or specialized components (e.g., automotive semiconductors, medical devices) require more intricate design and materials, costing $500 to $2,000 or more per unit.
  • Substrate Material: FR-4 boards are the most cost-effective option, while ceramic and metal-core substrates increase costs by 30% to 100%. The choice of material depends on the testing environment and component requirements, with high-temperature applications requiring more expensive materials.
  • Customization: Customized boards, tailored to specific component form factors or testing parameters, cost more than standard designs. Customization costs include engineering time, tooling, and prototype development, which can add $200 to $1,000 per board.
  • Order Quantity: Bulk orders reduce per-unit costs significantly. Ordering 10 or more boards can lower per-unit costs by 20% to 40% compared to single-unit orders. Manufacturers often offer volume discounts for large orders, making it more cost-effective to stock boards for ongoing testing needs.
  • Additional Features: Boards with built-in sensors, modular components, or advanced thermal management systems cost more. For example, a board with temperature sensors and real-time monitoring capabilities may cost 50% more than a basic board without these features.
  • Manufacturing Tolerances: Tighter manufacturing tolerances, required for high-precision testing, increase costs. For example, boards with precise trace spacing or impedance control may cost 25% to 50% more than standard-tolerance boards.

What Should You Look for When Choosing a Reliable Burn in Board Manufacturer?

Selecting a reliable burn in board manufacturer is critical to ensuring consistent testing results, on-time delivery, and long-term product reliability. The following factors help identify manufacturers that can meet your specific needs and deliver high-quality boards.

  • Industry Experience: Look for manufacturers with a proven track record in producing burn in boards for your industry. Experience with automotive, medical, or industrial components ensures the manufacturer understands the unique testing requirements and standards for your application.
  • Quality Control Processes: Reliable manufacturers implement strict quality control processes, including incoming material inspection, in-process testing, and final validation. Ask about their quality management system, such as ISO 9001 certification, and request documentation of test results for their boards.
  • Customization Capabilities: Choose a manufacturer that can customize boards to your specific component and testing requirements. This includes the ability to design boards for unique form factors, adjust thermal management systems, and integrate specialized features like sensors or monitoring tools.
  • Material Sourcing: Ensure the manufacturer uses high-quality, industry-approved materials for board construction. Ask about their material suppliers and verify that they use genuine, certified materials to avoid performance issues or premature board failure.
  • Delivery Timeframes: On-time delivery is critical to maintaining production schedules. Look for manufacturers with a reputation for meeting delivery deadlines, even for custom orders. Ask about their lead times and contingency plans for unexpected delays.
  • Technical Support: A reliable manufacturer provides ongoing technical support, including assistance with board design, testing optimization, and troubleshooting. This ensures you can resolve any issues quickly and maximize the performance of your burn in boards.
  • Pricing Transparency: Choose a manufacturer that provides clear, detailed pricing with no hidden fees. Ask for a breakdown of costs, including design, materials, manufacturing, and shipping, to ensure you can budget effectively and avoid unexpected expenses.
Burn in Board, https://www.bestpcbs.com/blog/2026/05/burn-in-board/

What is the Correct HS Code for Burn in Boards for Import and Export?

The primary HS code for burn in boards is 8534.00.90. This code covers printed circuit boards (PCBs) that are not specifically classified under other subheadings, including specialized boards used for testing, such as burn in boards. This code applies to both single-layer and multi-layer burn in boards, regardless of their design complexity or customization.

It is important to note that HS codes may vary slightly by country or region, so it is recommended to verify the code with local customs authorities before importing or exporting. Some countries may classify burn in boards under subheadings of 8534.00, depending on factors like material composition (e.g., ceramic vs. FR-4) or intended use.

When completing customs documentation, provide a detailed description of the burn in board, including its purpose (reliability testing of electronic components), material composition, and design features. This ensures customs officials can verify the correct classification and avoid delays or penalties.

FAQs About Burn in Board

Q1: Can burn in boards be reused for different component types?

A1: Yes, many burn in boards are designed with modular components or interchangeable connectors, allowing them to be reused for different component types. Modular designs reduce the need for multiple dedicated boards, saving costs and storage space. However, reuse requires reconfiguration to match the new component’s electrical and physical requirements, including adjusting trace spacing, voltage settings, and component mounting points.

Q2: How long does a typical burn in test with a burn in board take?

A2: The duration of a burn in test varies based on component type and industry standards. Most tests last between 24 and 168 hours. Consumer electronics components often require 24 to 48 hours of testing, while automotive and medical components may need 72 to 168 hours to ensure long-term reliability. The goal is to apply enough stress to reveal early failures without damaging functional components.

Q3: Do all electronic components require burn in testing with a burn in board?

A3: No, not all components require burn in testing. Low-cost, low-reliability components (e.g., basic resistors for toys) may not need testing, as the cost of testing outweighs the risk of failure. However, components used in critical applications (automotive, medical, aerospace) or high-value products (servers, industrial equipment) almost always require burn in testing to ensure reliability and compliance with industry standards.

You may also like

550mm to Inches | Simple Conversion for Engineering Sizes

May 7th, 2026

What Is 550mm to Inches?

550mm to inches equals 21.6535 inches. If you need a clean rounded value, 550mm is usually written as 21.65 inches. For casual product descriptions, it can also be written as about 21.7 inches. However, for engineering drawings, PCB panel dimensions, mechanical parts, fixtures, and assembly work, it is better to keep the exact millimeter value or use the more accurate inch conversion.

The calculation is simple:

550 ÷ 25.4 = 21.6535 inches

This is because 1 inch equals exactly 25.4 millimeters. So, when you convert millimeters to inches, you divide the millimeter value by 25.4.

550mm to Inches | Simple Conversion for Engineering Sizes

What Is 1 Inch Equal to in mm?

1 inch is equal to exactly 25.4mm. This is the standard conversion factor used for all inch-to-millimeter and millimeter-to-inch calculations. So, when you want to convert inches to millimeters, you multiply the inch value by 25.4. When you want to convert millimeters to inches, you divide the millimeter value by 25.4.

For example:

InchesMillimeters
1 inch25.4mm
2 inches50.8mm
5 inches127mm
10 inches254mm
21.65 inchesAbout 550mm

In PCB drawings, mechanical parts, enclosure design, and product specifications, this conversion factor is very important. A small rounding mistake can affect size matching, assembly clearance, fixture design, and packaging accuracy.

What Is the Formula to Convert 550mm to Inches?

The formula is: inches = millimeters ÷ 25.4. For 550mm, the calculation is:

550 ÷ 25.4 = 21.6535433071 inches

Rounded to two decimal places, the answer becomes 21.65 inches.

This formula works for any millimeter-to-inch conversion. You only need to replace 550 with the millimeter value you want to convert.
MillimetersFormulaInches
100mm100 ÷ 25.43.94 in
250mm250 ÷ 25.49.84 in
400mm400 ÷ 25.415.75 in
550mm550 ÷ 25.421.65 in
650mm650 ÷ 25.425.59 in
1000mm1000 ÷ 25.439.37 in

This formula is especially useful when working with drawings or specifications that mix metric and imperial values. In PCB manufacturing, for example, a customer may submit a board outline in millimeters, while an enclosure drawing or panel fixture may be discussed in inches. Using the correct formula prevents mismatch between design intent and production output.
Is 550mm the Same as 21.65 Inches?

Yes, 550mm is commonly written as 21.65 inches when rounded to two decimal places. The exact result is slightly longer: 21.6535 inches. The difference between 21.65 and 21.6535 inches is extremely small, so 21.65 inches is suitable for many general and technical descriptions.
However, the right level of rounding depends on the application.

For example, if you are describing the approximate width of a product on a webpage, 21.65 inches is fine. If you are preparing a PCB production drawing, panel layout, SMT stencil drawing, CNC fixture, or inspection jig, you should keep the original metric value and add inches only as a reference.

A good engineering format is:

550mm / 21.6535 in

A good product description format is:

550mm / 21.65 in

A good casual description format is:

About 21.7 inches

The more precise the part, the more carefully the conversion should be written.

Should 550mm Be Rounded to 21.7 Inches or 22 Inches?

550mm can be rounded to 21.7 inches for general reading, but it should not be rounded to 22 inches for engineering use. The value 22 inches is only an approximation. It is easy to read, but it is not dimensionally accurate.

The exact value is 21.6535 inches. If you round it to one decimal place, it becomes 21.7 inches. If you round it to the nearest whole inch, it becomes 22 inches. The problem is that 22 inches is actually 558.8mm, which is about 8.8mm larger than 550mm.

That difference may be acceptable for a rough estimate, but it can be too large for PCB, enclosure, display, fixture, or mechanical assembly applications.

Rounded FormatInch ValueDifference from Exact ValueBest Use
Exact value21.6535 in0Engineering data
2 decimals21.65 inVery smallProduct specifications
1 decimal21.7 inAbout 0.0465 inGeneral reading
Whole inch22 inAbout 0.3465 inRough estimate only
22 inches in mm558.8mm8.8mm larger than 550mmNot suitable for precision

For PCB-related work, 8.8mm is not a small deviation. It can affect panel arrangement, board fitting, tooling holes, fixture size, packaging clearance, and final assembly compatibility.

How Long Is 550mm in Real Life?

550mm is 55cm, 0.55m, or about 21.65 inches. In feet and inches, it is about 1 foot and 9.7 inches.

This length is a little under 2 feet. It is longer than a standard sheet of paper and close to the width or length of many electronic assemblies, equipment housings, display modules, tooling frames, and medium-sized panels.
To make the size easier to imagine:

Metric SizeImperial SizePractical Feeling
550mm21.65 inchesA little less than 2 feet
550mm55cmSlightly over half a meter
550mm0.55mMedium product dimension
550mm1 ft 9.7 inCommon for panels or frames

In electronics, 550mm may appear in several places. It could be the length of a PCB production panel, a fixture base, a stencil frame, a machine working area, a cable harness reference, or the outer size of a device enclosure. Because the number is large enough to affect manufacturing efficiency, it should be converted carefully.

What Is 550mm in Feet and Inches?

550mm is about 1 foot and 9.7 inches. This format is useful when communicating with people who prefer imperial measurements.

The calculation works like this:

550mm equals 21.6535 inches.
There are 12 inches in 1 foot.
21.6535 inches equals 1 foot plus 9.6535 inches.

So the practical result is:

550mm = about 1 ft 9.7 in

Millimeter ValueInchesFeet and Inches
300mm11.81 in0 ft 11.8 in
450mm17.72 in1 ft 5.7 in
550mm21.65 in1 ft 9.7 in
650mm25.59 in2 ft 1.6 in
800mm31.50 in2 ft 7.5 in

This format is helpful for general communication, but it is not ideal for production drawings. Manufacturing teams usually prefer decimal inches or millimeters because they are easier to measure and control.

How Do You Convert Millimeters to Inches Step by Step?

To convert millimeters to inches, divide the millimeter value by 25.4. For 550mm, the answer is 21.6535 inches.

Here is the step-by-step process:

Step 1: Write the millimeter value
The value is 550mm.

Step 2: Use the conversion factor
1 inch = 25.4mm.

Step 3: Divide by 25.4
550 ÷ 25.4 = 21.6535433071.

Step 4: Round the result
For most uses, write it as 21.65 inches.

Step 5: Choose the right precision
Use more decimal places for engineering work. Use fewer decimal places for general reading.

This same method works for any size. For example, 650mm to inches is 650 ÷ 25.4 = 25.59 inches. A 450mm measurement equals 17.72 inches.

What Is 550mm × 650mm in Inches?

550mm × 650mm equals approximately 21.65 inches × 25.59 inches. This type of conversion is useful for PCB panels, SMT stencil frames, machine working areas, packaging boxes, aluminum plates, display modules, and mechanical enclosures.

What Is 550mm × 650mm in Inches?

For rectangular sizes, convert each side separately:

550 ÷ 25.4 = 21.65 inches
650 ÷ 25.4 = 25.59 inches

So:

550mm × 650mm = 21.65 in × 25.59 in

Metric SizeInch SizeRounded Size
550mm × 550mm21.65 in × 21.65 in21.7 in × 21.7 in
550mm × 650mm21.65 in × 25.59 in21.7 in × 25.6 in
450mm × 550mm17.72 in × 21.65 in17.7 in × 21.7 in
370mm × 470mm14.57 in × 18.50 in14.6 in × 18.5 in
300mm × 550mm11.81 in × 21.65 in11.8 in × 21.7 in

Why Does 550mm to Inches Matter in PCB and Electronics Manufacturing?

550mm to inches matters because PCB and electronics projects often move between metric and imperial dimensions. A board outline may be designed in millimeters, while an enclosure, equipment drawing, customer requirement, or packaging specification may refer to inches.

In PCB manufacturing, 550mm may relate to:

  • PCB production panel length or width
  • SMT stencil size
  • Reflow carrier fixture size
  • Wave solder pallet size
  • CNC routing working area
  • Electrical test fixture base
  • Packaging carton dimension
  • Large-format LED, power, or industrial control boards
  • Mechanical enclosure matching
  • Assembly line handling clearance

For example, if a PCB panel is designed as 550mm wide, the inch equivalent is 21.65 inches. If someone rounds it to 22 inches during communication, the difference becomes 8.8mm. That may influence panelization, fixture compatibility, or packaging accuracy.

550mm to inches in pcb manufacturing

What Mistakes Should You Avoid When Converting 550mm to Inches?

The most common mistake is rounding 550mm to exactly 22 inches and treating it as a precise value. It is close, but not exact. Another common mistake is confusing millimeters with centimeters.

Here are the main errors to avoid:

MistakeWhy It MattersBetter Practice
Writing 550mm as exactly 22 inches22 inches is 558.8mm, not 550mmUse 21.65 inches
Confusing mm and cm550mm is 55cm, not 550cmCheck unit labels carefully
Using 2.54 for mm conversion2.54 is centimeters per inchUse 25.4 for millimeters
Removing decimals in drawingsMay affect fit, clearance, or toolingKeep accurate values
Ignoring toleranceReal parts have manufacturing variationAdd tolerance where needed
Mixing rounded and exact valuesCan confuse suppliers and inspectorsDefine one primary unit

For PCB and PCBA projects, the safest approach is to keep the original design unit as the master value. If the original file, Gerber data, mechanical drawing, or fabrication note uses millimeters, the inch value should be treated as a reference unless otherwise specified.

How Should You Write 550mm in Product Specifications?

The best product specification format is 550mm / 21.65 inches. This is clear, accurate, and easy for international readers to understand.

A clean product description might look like this:

Length: 550mm / 21.65 in

For a more detailed technical drawing, you can write:

Length: 550.00mm [21.6535 in]

For a general sales page, you can write:

Approx. 550mm / 21.7 in

In PCB manufacturing, consistency is very important. If the drawing uses millimeters, keep all related dimensions in millimeters. If inches are added, label them clearly as reference values.

What Are Similar Millimeter to Inch Conversions?

Similar conversions help users compare 550mm with nearby sizes. This is useful when selecting a panel size, enclosure, rack, fixture, or product housing.

MillimetersInchesRounded Value
500mm19.6850 in19.69 in
520mm20.4724 in20.47 in
540mm21.2598 in21.26 in
550mm21.6535 in21.65 in
560mm22.0472 in22.05 in
580mm22.8346 in22.83 in
600mm23.6220 in23.62 in

FAQs

1. How many inches is 550mm?

550mm is 21.6535 inches. Rounded to two decimal places, it is 21.65 inches.

2. Is 550mm equal to 22 inches?

No. 550mm is about 21.65 inches. By comparison, 22 inches equals 558.8mm, which is about 8.8mm longer than 550mm.

3. What is 550mm in feet and inches?

550mm is about 1 foot and 9.7 inches. This format is helpful for general size comparison.

4. What is the formula for converting 550mm to inches?

The formula is:

inches = millimeters ÷ 25.4

So: 550 ÷ 25.4 = 21.6535 inches

5. Is 550mm the same as 55cm?

Yes. 550mm equals 55cm, because 10mm equals 1cm.

6. Should PCB drawings use 550mm or 21.65 inches?

PCB drawings should usually keep 550mm as the primary dimension if the design was created in metric units. The inch value, 21.65 inches, can be added as a reference for international communication.

7. Is 21.65 inches accurate enough for 550mm?

For most product specifications, yes. 21.65 inches is accurate enough for general use. For high-precision engineering, use 21.6535 inches or keep the original 550mm value.

8. What is 550mm × 650mm in inches?

550mm × 650mm equals approximately 21.65 inches × 25.59 inches. This size format is common in panels, frames, fixtures, and packaging dimensions.

You may also like

Best Metal Core Circuit Board Manufacturer in China | Thermal Solution

May 6th, 2026

Are you struggling with overheating, signal instability, low yield, or long lead time in your metal core circuit board projects? This guide breaks down real-world pain points in design, prototyping, and assembly, shares proven solutions, and shows how EBest delivers reliable, high-performance metal core circuit board and metal core printed circuit board solutions for LED, medical, aerospace, and industrial applications. We combine 20+ years of expertise, strict certifications, and one-stop services to solve your thermal and reliability challenges.

Metal Core Circuit Board, https://www.bestpcbs.com/blog/2026/05/metal-core-circuit-board-2/

What Are the Pain Points in Metal Core Circuit Board Design and How Do We Solve Them?

Metal core circuit board design often brings thermal, electrical, and manufacturability conflicts. Below we list the most common pain points and our targeted engineering fixes.

  • Poor thermal conductivity causing overheating in high‑power devices: We optimize dielectric layer thickness and metal substrate selection to boost heat dissipation.
  • Signal interference and crosstalk in dense layouts: We use grounded metal cores and impedance matching to stabilize signal integrity.
  • Complex DFM rules leading to low yield: Our engineers provide early design reviews and standardized design guidelines.
  • Warpage and deformation under thermal cycles: We balance material CTE and apply structural reinforcement in layout.
  • Insulation breakdown risk at high voltage: We use high‑quality dielectric materials and strict creepage/clearance control.
  • Difficulty integrating HDI structures: We combine laser drilling and metal core processing for reliable HDI integration.

What Are the Challenges in Metal Core Circuit Board Prototype and How Do We Fix Them?

Prototyping metal core printed circuit boards often means tight deadlines, inconsistent quality, and high costs. Here’s how we eliminate those hurdles.

  • Long lead times delaying product development: We offer 24-hour rapid prototyping for urgent metal core circuit board projects.
  • Inconsistent performance between prototype and mass production: We use stable production lines and unified materials for prototypes.
  • High cost for small‑batch prototypes: We provide flexible MOQ and cost‑effective prototype solutions.
  • Poor dimensional accuracy in complex structures: We apply precision machining and online inspection throughout production.
  • Material compatibility failures: We pre‑test metal substrates, dielectrics, and copper foils for reliability.
  • Limited prototype customization: We support single‑sided, double‑sided, and multilayer custom prototypes.

What Are the Problems in Metal Core Circuit Board Assembly and How Do We Solve Them?

Assembly of metal core printed circuit boards involves unique thermal and mechanical stresses. We address every common failure point to ensure robust, long‑lasting assemblies.

  • Component damage from excessive heat during soldering: We use controlled reflow profiles and thermal buffer designs.
  • Poor solder wetting on metal core boards: We optimize surface finishes and pre‑treat metal substrates.
  • Thermal stress causing delamination or cracking: We match CTE and reinforce key assembly areas.
  • Difficulty with thick or heavy boards: We provide rigid support fixtures and professional assembly lines.
  • Insulation defects after assembly: We perform 100% electrical and hi‑pot testing.
  • Low efficiency in mixed assembly: We integrate SMT, through‑hole, and connector assembly in one stop.

Why Choose EBest as Your Metal Core Circuit Board Manufacturer in China?

EBest focuses on services that directly improve your product performance, speed, and reliability. We deliver end-to-end support for your metal core circuit board needs.

  • Professional metal core circuit board design review & DFM optimization: Our experienced engineers conduct comprehensive design audits to identify potential manufacturability issues (such as acid traps or weak annular rings) in advance,lowering production failure rates, reducing rework costs, and ensuring your project stays on budget and on schedule.
  • Rapid 24-hour prototyping for metal core printed circuit boards: We prioritize your R&D timeline with urgent prototyping services, speeding up your product development cycle, helping you test and validate designs faster, and gaining a competitive edge in the market.
  • Full-process assembly (SMT + through-hole + testing) for one-stop project delivery: We integrate all assembly processes in-house, eliminating handovers between multiple factories, shortening lead times, reducing quality variation risks, and saving you time and effort in coordinating multiple suppliers.
  • Custom material matching (aluminum/copper/alloy) for ideal thermal performance: We tailor substrate material selection to your specific project needs, ensuring optimal heat dissipation, improving the stability and lifespan of your end products, and avoiding overheating-related failures.
  • Strict quality control with IATF 16949, ISO 9001, ISO 13485, AS9100D, RoHS, REACH, UL: Our certified quality management system covers every production step, guaranteeing consistent product quality, ensuring compliance with global industry standards, and giving you confidence in using our products in regulated industries like medical, aerospace, and automotive.
  • Stable mass production with consistent quality from prototype to volume: We maintain unified production processes and material standards for both prototypes and mass production, ensuring no performance differences between small-batch samples and large-volume orders, stabilizing your per-unit costs, and supporting your long-term production planning.
  • Thermal simulation & reliability testing to validate performance before shipment: We conduct rigorous thermal and reliability tests prior to delivery, identifying potential performance issues in advance, ensuring your metal core circuit boards meet design expectations, and reducing post-delivery maintenance costs.
  • Flexible order quantities from samples to mass production: We support small-batch samples, medium-volume orders, and large-scale mass production, accommodating your project’s different stages, reducing your initial investment risk, and scaling seamlessly with your business growth.
  • 24/7 technical support from layout to after-sales: Our professional technical team is available around the clock, providing timely guidance from design layout to after-sales use, solving your technical problems quickly, and ensuring your project progresses smoothly without delays.

What Types of Metal Core Printed Circuit Boards Can EBest Provide?

We support standard and custom configurations to match your thermal, electrical, and mechanical needs.

  • Single sided metal core printed circuit board
  • Double sided metal core printed circuit board
  • Customized multilayer metal core circuit boards PCB
  • High thermal conductivity metal core printed circuit boards
  • Heavy copper metal core printed circuit board
  • High‑TG metal core printed circuit boards
  • Thin metal core printed circuit board for compact devices
metal core circuit board, https://www.bestpcbs.com/blog/2026/05/metal-core-circuit-board-2/

What Qualifications Should a Reliable Metal Core Circuit Board Manufacturer Have?

A trusted provider must meet industry, quality, and technical benchmarks to ensure safe, consistent metal core circuit board production.

  • ISO 9001 quality management system
  • IATF 16949 for automotive, ISO 13485 for medical, AS9100D for aerospace
  • RoHS and REACH compliance for environmental safety
  • UL safety certification for global markets

How Does EBest Ensure Superior Thermal Conductivity in Metal Core Circuit Boards?

We use a full-system, engineering-driven approach to maximize heat dissipation in every metal core circuit board, addressing material selection, design, production, and testing to ensure superior thermal conductivity. Below are our key steps, detailed yet concise:

  • Customized Metal Substrate Selection: We select high-purity aluminum, copper, or alloy substrates based on your specific thermal demand. Aluminum substrates (150–240 W/mK) offer cost-effective thermal performance for most applications, while copper substrates (385–400 W/mK) deliver maximum heat dissipation for ultra-high-power scenarios, ensuring optimal heat transfer from components to the heat sink.
  • High-K Dielectric Layer Optimization: We use high-k dielectric materials (k value 6–100+) with thermal conductivity of 3.0–8.0 W/(m・K) — far superior to standard FR-4 (0.3–0.4 W/mK) to balance low thermal resistance and high insulation. This ensures efficient heat transfer while preventing electrical breakdown[superscript:2].
  • Precise Dielectric Thickness Control: We precisely adjust dielectric layer thickness (typically 50–200 μm) to strike the perfect balance between heat transfer and voltage safety. Thinner layers reduce thermal resistance, while ensuring adequate breakdown voltage to meet your project’s electrical requirements.
  • High-Density Thermal Via Design: We deploy high-density thermal via arrays with thermally conductive resin plugging to eliminate heat accumulation points. These vias create direct heat paths from components to the metal core, minimizing thermal bottlenecks and ensuring uniform heat distribution across the board.
  • Thermal Simulation & Layout Optimization: Before production, we use thermal simulation tools to optimize component placement and heat dissipation paths. We position high-power components over metal core areas and avoid heat coupling, ensuring efficient heat spread and preventing hotspots that degrade performance.
  • Void-Free Vacuum Lamination: We use stable vacuum lamination with controlled pressure to eliminate microscopic air gaps (which act as thermal insulators). This ensures consistent bonding between layers, minimizing interface thermal resistance and maximizing heat transfer efficiency.
  • 100% Pre-Shipment Thermal & Electrical Testing: Every metal core circuit board undergoes rigorous thermal conductivity and electrical tests before shipment. We verify thermal performance meets design specifications, ensuring no defects and guaranteeing consistent, reliable heat dissipation for your end products.
metal core circuit board, https://www.bestpcbs.com/blog/2026/05/metal-core-circuit-board-2/

EBest’s Metal Core Circuit Board for LED Lighting Industry Case Study

This real-world case demonstrates how our metal core circuit board solutions address core pain points of high-power LED lighting, delivering tangible value for our clients. We focus on practical, results-driven solutions tailored to LED lighting industry needs.

Project Background

Our client, a global LED lighting manufacturer, had critical issues with their high-power LED streetlights: severe heat buildup in the closed lamp housing caused rapid lumen decay (30% within 6 months), frequent dead lights, and a shortened service life (under 20,000 hours), damaging their reputation and increasing after-sales costs.

Project Requirements

The client’s core needs centered on resolving heat-related failures and ensuring market competitiveness, with clear, measurable goals:

  • Resolve heat dissipation issues to ensure stable long-term operation of LED streetlights.
  • Extend the LED streetlight service life to over 50,000 hours (a standard benchmark for high-quality LED lighting).
  • Reduce lumen decay to less than 10% within 2 years (far below the industry average for poorly cooled products).
  • Completely eliminate dead light problems caused by overheating.
  • Maintain compliance with RoHS and UL standards to ensure global market access.

Our Solution

We customized a high-thermal metal core printed circuit board specifically tailored to their LED streetlight specifications, addressing every heat dissipation pain point with targeted engineering:

  • Substrate selection: Chose high-purity 1060 aluminum substrates (with excellent thermal conductivity of 205W/(m・K)) to accelerate heat transfer from LED chips to the heat sink.
  • Dielectric layer optimization: Set dielectric layer thickness to 0.15mm and used high-k dielectric materials (thermal conductivity 3.0-4.0W/(m・K)) to balance heat dissipation and insulation performance, reducing thermal resistance by 50% compared to standard materials.
  • Thermal via design: Added high-density thermal via arrays with resin plugging to eliminate heat accumulation points, ensuring uniform heat distribution across the board.
  • Layout & validation: Optimized the board layout to avoid heat coupling between components, conducted pre-production thermal simulations to verify design effectiveness, and provided 24-hour rapid prototyping for quick validation of performance.

Project Results

After mass production and on-site testing, the LED streetlights equipped with our metal core printed circuit boards delivered tangible, measurable improvements for the client:

  • Temperature control: Stable operating temperatures reduced by 25℃ compared to the client’s previous solution, keeping LED chip junction temperature below 70℃ (the threshold for avoiding accelerated lumen decay).
  • Lumen decay & lifespan: Lumen decay was controlled within 8% after 2 years of continuous operation, and service life extended to 55,000 hours (exceeding the client’s 50,000-hour requirement).
  • Reliability improvement: Dead light issues were completely eliminated, reducing the client’s after-sales maintenance costs by 40%.
  • Market compliance: The product fully met RoHS and UL standards, helping the client expand their global market share and enhance brand credibility.

What Should You Look for When Choosing a Metal Core Circuit Board Manufacturer?

Focus on these critical factors to select a partner that delivers consistent, high‑quality metal core circuit board solutions.

  • Strong thermal design and testing capabilities: Prioritize manufacturers with professional thermal design teams and advanced testing equipment. They should offer thermal simulation services to optimize metal core circuit board layout and heat dissipation paths, and have in-house labs to conduct thermal conductivity, thermal cycling, and insulation tests, this ensures the board meets your heat management needs and avoids overheating-related failures.
  • Complete industry certifications matching your target market: Certifications are non-negotiable for reliability and market access. Ensure the manufacturer holds ISO 9001 (basic quality), plus industry-specific certifications: IATF 16949 (automotive), ISO 13485 (medical), AS9100D (aerospace), as well as RoHS, REACH, and UL compliance to meet global regulatory requirements.
  • One-stop service covering design, prototyping, assembly, and mass production: Choose a manufacturer that offers end-to-end services to avoid coordination hassle between multiple suppliers. This includes DFM design reviews, rapid prototyping, SMT/through-hole assembly, and mass production, which shortens lead times, reduces quality inconsistencies, and saves you time and costs.
  • Consistent quality between prototype and mass production: Inconsistent performance between samples and bulk orders is a common pain point. Verify the manufacturer uses unified materials, production processes, and quality control standards for both prototypes and mass production to ensure stable product performance and avoid rework or product failures post-launch.
  • Flexible customization for special requirements: Your metal core circuit board may need custom specifications (e.g., single/double/multilayer structures, heavy copper, thin boards, or high-TG materials). The manufacturer should accommodate custom material selection, layer designs, and dimensional requirements to match your specific product needs.
  • Fast, reliable lead times and urgent order support: Timely delivery is critical for your R&D and production schedules. Look for manufacturers that offer 24-hour rapid prototyping for urgent projects and have stable production capacity to meet your mass production deadlines, even during peak periods.
  • Transparent quality control (QC) processes and test reports: A reliable manufacturer will have transparent QC processes covering every production step from material inspection to final shipment. They should provide detailed test reports (thermal, electrical, reliability) to prove product quality, giving you confidence in the boards you receive.
  • Experienced engineering and after-sales support: Optimize for a manufacturer with a professional engineering team that can provide timely guidance from design layout to problem-solving. 24/7 after-sales support is also essential to resolve any issues (e.g., performance discrepancies) quickly and avoid project delays.
Metal Core Circuit Board, https://www.bestpcbs.com/blog/2026/05/metal-core-circuit-board-2/

FAQs About Metal Core Circuit Board

Q1: What is the current trend in the metal core printed circuit board market? A1: The metal core printed circuit board market is growing rapidly, driven by LED, automotive, industrial, and 5G applications. Demand is rising for higher thermal conductivity, thinner structures, heavy copper, and multilayer designs.

Q2: What factors affect metal core printed circuit board performance? A2: Key factors include metal substrate type, dielectric material, layer structure, thermal design, production process, and assembly quality.

Q3: What is the difference between aluminum and copper metal core printed circuit boards? A3: Aluminum offers good thermal performance at a lower cost; copper provides higher thermal conductivity for ultra‑high‑power applications.

Q4: Can metal core printed circuit boards be used in high‑frequency devices? A4: Yes, with optimized dielectric and layout, metal core circuit board supports high‑frequency and RF applications.

Q5: Are metal core printed circuit boards suitable for mass production? A5: Yes, EBest provides stable mass production for metal core printed circuit boards with consistent quality.

Q6: How to improve thermal performance of a metal core printed circuit board? A6: Optimize substrate material, dielectric layer, thermal vias, component layout, and heat sink design.

Q7: What industries use metal core printed circuit boards most? A7: LED lighting, automotive electronics, industrial power, medical devices, aerospace, and 5G communications.

Contact EBest for Your Metal Core Circuit Board Needs

EBest is a leading metal core circuit board manufacturer in China, providing professional custom thermal solutions. We support design, prototyping, assembly, and mass production for global clients. For inquiries about metal core printed circuit boards, please contact us at: sales@bestpcbs.com.

You may also like