Reliable PCB board soldering depends on controlled heat, compatible materials, and clean joining surfaces. Too little heat prevents proper wetting, while prolonged contact can damage the pad or laminate.
This guide explains the main soldering methods and the temperatures used for each process. It also covers hand soldering, cleaning, common defects, and the point at which production equipment becomes the better choice.
What Is PCB Board Soldering?
PCB board soldering is the process of using solder to attach an electronic component to a printed circuit board. It creates an electrical path for current and a mechanical bond that holds the component in place.
The component termination is the metal lead or contact that joins the board, while the PCB pad is the exposed copper area beneath it. During soldering, both surfaces are heated together and flux removes light oxidation, allowing solder to spread across both metals. This spreading action is called wetting and shows that the solder has bonded to the surfaces.
Types of PCB Soldering
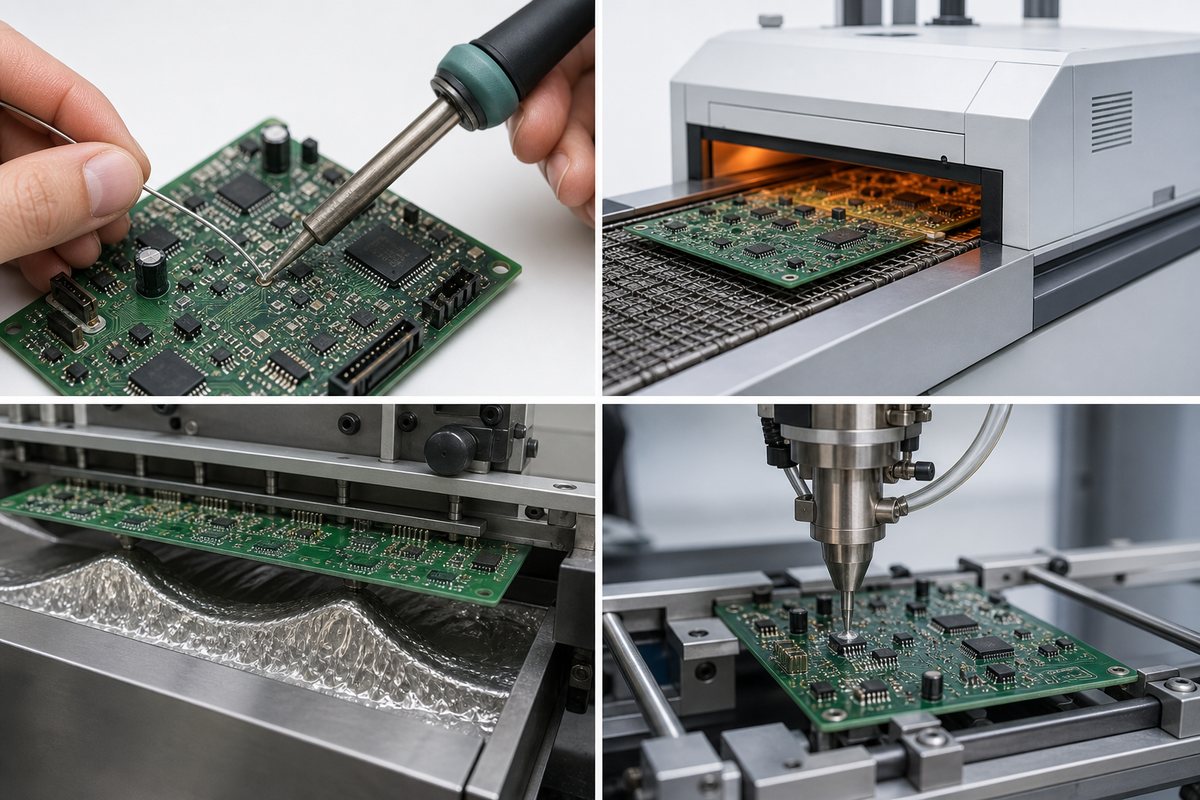
The main types of PCB soldering are manual, reflow, wave, and selective soldering. The right method depends mainly on the components and the number of boards being assembled.
Method
Typical Application
Solder Form
Manual soldering
Prototypes, wires, through-hole parts, and rework
Flux-cored solder wire
Reflow soldering
Surface-mount components on assembled panels
Solder paste
Wave soldering
Repeated through-hole assembly
Molten solder bath
Selective soldering
Localized through-hole joints on mixed assemblies
Molten solder from a controlled nozzle
Most SMT production uses reflow, while wave and selective systems handle through-hole connections efficiently. A mixed assembly may pass through reflow first, then receive selective soldering for connectors or power components. This wave soldering guide explains the through-hole process in more detail.
What Tools Do You Need for PCB Board Soldering?
A basic PCB soldering setup only needs a few essential tools, and each tool supports a different part of the job. The following items make beginner work safer and easier to control:
Temperature-controlled soldering station: keeps the tip near the selected temperature and provides a safe stand.
Small and medium chisel tips: provide enough contact area for both small pads and larger joints.
Solder wire and flux: form the joint and help the solder spread across clean metal.
PCB holder and ESD-safe tweezers: keep the board and component steady while both hands remain free.
Tip cleaner and flux remover: maintain heat transfer and remove unwanted residue after soldering.
Magnification and fume extraction: improve inspection and keep fumes away from the work area.
This equipment is enough for most beginner hand-soldering work. Surface-mount production needs a different setup because many small components are placed and heated together. Solder paste is printed through a PCB stencil, components are positioned on the wet paste, and a controlled oven then reflows every joint.
How Should You Choose a PCB Board Soldering Iron?
Choose a temperature-controlled PCB board soldering iron with interchangeable tips, and make sure it recovers heat quickly after touching a joint. This ability is called thermal recovery, and it keeps the tip from becoming too cool during soldering.
The tip should contact the pad and component lead at the same time without touching neighboring conductors. A small chisel tip usually transfers heat more efficiently than a needle point. Larger chisel tips suit connectors, ground planes, and other high-copper areas.
Which Solder Wire and Flux Work Best for Circuit Boards?
Electronics-grade solder wire with a compatible flux core works best for most hand-soldered circuit boards. Solder wire supplies the metal alloy, while flux cleans the heated surfaces and helps that alloy spread.
Thin wire gives better volume control on dense boards, while thicker wire feeds larger through-hole joints faster. Tin-lead solder wets readily at lower temperatures. Many products, however, require a lead-free alloy such as SAC or tin-copper. Never use plumbing solder or acid flux because the residue can attack an electronic assembly.
What PCB Board Soldering Temperature Should You Use?
PCB board soldering temperature commonly falls around 315–370°C for hand soldering, while lead-free reflow profiles often peak near 230–250°C. These ranges are starting points rather than fixed settings for every board.
The required temperature changes with the solder alloy and the amount of copper around the joint. SAC lead-free solder melts around 217–220°C, but an iron tip must be hotter so it can transfer heat into the metals. Small pads warm quickly, while large copper areas pull heat away from the tip.
How to do Soldering on PCB Board?
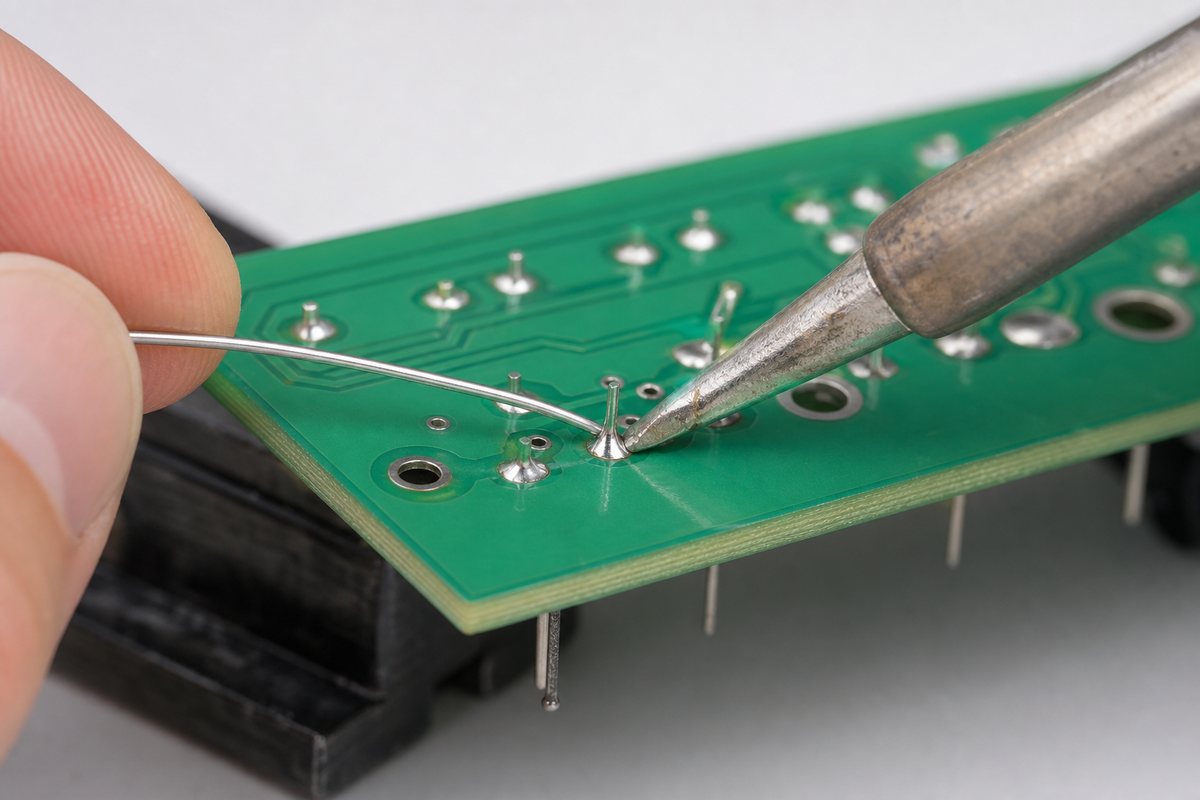
The PCB board soldering process begins with a clean, stable connection and ends with an undisturbed joint. Follow this sequence so the lead and pad receive heat together:
Disconnect power, discharge stored energy, and secure the PCB.
Confirm the component value, orientation, polarity, and lead position.
Clean and tin the iron tip, then apply suitable flux if required.
Place the tip where it touches both the pad and component lead.
Feed a small amount of solder into the heated joint, not onto the tip.
Remove the solder wire first, then lift away the iron.
Keep the connection still while it cools, then inspect the joint.
After the joint cools, the solder should remain around the lead and within the copper pad. If it does not form after a short heating period, stop instead of repeatedly reheating the area. First clean the surfaces and inspect the tip, then decide whether more flux or a larger tip is needed.
How to Clean PCB Board After Soldering?
Clean a PCB after soldering when the flux chemistry or product requirements call for it. Disconnect power and let the board cool before choosing a cleaner, because different flux residues require different removal methods.
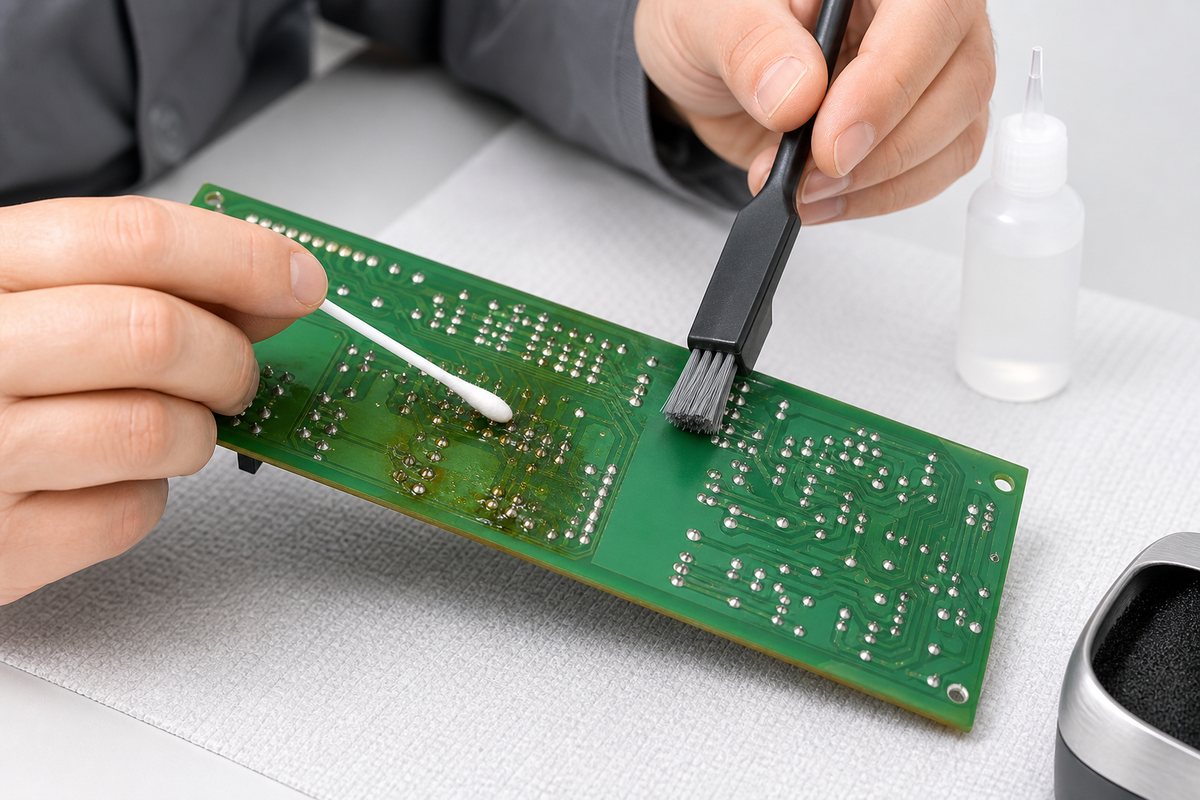
Once the correct cleaner has been selected, use the following sequence to remove residue without spreading it across the board:
Apply an approved electronics cleaner or high-purity isopropyl alcohol.
Agitate the residue with a lint-free swab or ESD-safe brush.
Lift or rinse away the dissolved material instead of spreading it.
Avoid forcing liquid beneath switches, microphones, and unsealed parts.
Dry the assembly completely and inspect it under magnification.
The final inspection matters because simple wiping can dissolve flux and move it to another area. Activated and water-soluble residues usually need thorough removal, while permitted no-clean residue may remain on the board. Cleaning can still be necessary before conformal coating.
How Can You Recognize and Fix Poor Solder Joints?
Poor solder joints often show incomplete wetting or the wrong amount of solder. Cracks, bridges, and heat damage are also warning signs, and magnification makes them easier to see before electrical testing.
Each defect needs a different correction. Use the joint’s visible condition to choose the next step:
Cold or disturbed joint: remove contamination, add flux, and reheat both metals evenly.
Solder bridge: remove excess alloy with solder wick or controlled desoldering equipment.
Insufficient solder: reheat the joint and add only enough solder to complete the fillet.
Excess solder: remove enough material to reveal the joint shape and prevent hidden shorts.
Lifted pad or damaged barrel: stop heating and evaluate whether an approved conductor repair is possible.
After the repair, inspect the joint again before returning power to the board. Check that the intended connection has continuity and that neighboring conductors remain isolated. Lead-free joints can look duller than tin-lead joints, so shine alone does not prove quality.
Is It Okay to Put a Soldering Iron on a PCB Board?
Yes, the soldering tip may briefly touch the intended copper pad and component lead, but it should not rest elsewhere on the PCB. Keep it away from the solder mask and unrelated traces, and never use pressure to force heat into the joint.
Long contact can soften the adhesive beneath a copper pad and eventually lift it from the board. The surrounding mask or laminate may also darken and blister. Stop immediately when any of these signs appear.
A clean tip with the correct shape usually completes the joint faster than a tiny oxidized tip. Good thermal contact protects the PCB because the required energy enters the connection quickly, reducing total heating time.
When Is Manual Soldering No Longer Suitable?
Manual soldering is no longer suitable when joints are too small to reach reliably or are hidden beneath a component. It also becomes inefficient when the same connections appear across many boards. Fine-pitch SMT parts and BGA packages therefore usually require stencil printing, accurate placement, and controlled reflow.
Wave or selective soldering becomes more practical when a board contains many through-hole joints. These systems repeat the same heating and solder delivery conditions more consistently than hand work.
Manual soldering remains valuable for prototypes, wire connections, selected connectors, and controlled rework. Move to a machine process when many boards must receive the same thermal conditions and produce consistent inspection results.
FAQ About PCB Board Soldering
Why does solder form a ball instead of sticking to the PCB?
The pad may be oxidized, contaminated, or too cold. Clean the surface, use compatible flux, and heat the pad and lead together with a clean, tinned tip.
Should every solder joint look shiny?
No. Lead-free joints often look duller than tin-lead joints. Judge wetting, shape, cracks, bridges, and stability instead of using shine as the only acceptance criterion.
Can you solder wires directly to a PCB?
Yes, when the board has a suitable pad or plated hole and the wire receives strain relief. Avoid excessive solder wicking because it can make the wire rigid near the joint.
Do no-clean flux residues need to be removed?
Not always. Removal may still be necessary for appearance, high-impedance circuits, electrical testing, conformal coating, or environmental requirements defined by the product.
How long should a soldering iron touch a PCB pad?
Only long enough to produce full wetting, usually a few seconds during normal hand soldering. If the joint needs prolonged contact, stop and correct the heat-transfer problem.
Can you mix lead-free and tin-lead solder?
Mixing is sometimes possible during controlled repair, but it changes the alloy composition and melting behavior. Follow the assembly specification and avoid uncontrolled mixing.
Can a soldered PCB be tested immediately?
Inspect and clean the board first, then confirm that the joint has cooled and any cleaning liquid has fully evaporated. Check for bridges before applying power.
When should you stop repairing a solder joint?
Stop when the pad lifts, the plated hole loosens, the laminate chars, or repeated heating no longer restores a stable connection. Further work may cause permanent PCB damage.
How Can EBest Circuit Support PCB Assembly?
Reliable soldering begins with compatible component footprints and a suitable board finish. Clear assembly data then allows the production process to be set up correctly. EBest Circuit supports PCB fabrication and assembly from prototypes through production, with SMT, through-hole assembly, inspection, and engineering review available for suitable projects.
Send your Gerber files and BOM to sales@bestpcbs.com, together with the required quantity and any special soldering instructions. Placement data and assembly drawings will help our team review the package and discuss a practical manufacturing route.
Selecting SMD electronic components requires more than matching a value and package name. The chosen part must satisfy the circuit, fit the verified PCB footprint, survive the operating environment, remain available for production, and be compatible with placement, soldering, inspection and testing. A smaller or cheaper component is not a better choice if it reduces electrical margin, creates an uninspectable joint or introduces supply risk.
SMD means surface-mount device; SMT is the process used to assemble that device onto a PCB. Electrical and footprint decisions should be reviewed together with the manufacturer part number, lifecycle, traceability and approved alternatives. The most reliable result comes when the component and assembly process are evaluated as one system.
Which Requirements Should You Define Before Selecting SMD Electronic Components?
Begin with measurable product requirements, not a distributor filter. Define the circuit function, normal and worst-case loads, operating environment, board constraints, production volume and service life before comparing parts. Otherwise, an apparently suitable component may fail when temperature, transient energy or mechanical stress is considered.
Electrical conditions: Record nominal, minimum and maximum voltage, current, power, frequency, tolerance and transient conditions.
Mechanical limits: Define available board area, component height, connector forces, shock, vibration and enclosure constraints.
Environmental limits: Specify operating temperature, humidity, contamination exposure and any required product grade.
Production conditions: State prototype and forecast quantities, assembly sides, expected rework and inspection requirements.
How Do You Choose Between SMD, Through-Hole and Mixed PCB Assembly?
Match the assembly method to the product. Choose SMD for density and automated production, through-hole for selected mechanical or high-power needs, and mixed assembly when both are required. Make this decision before package selection because it affects layout, tooling, soldering and cost. Products with stressed connectors, large magnetic parts or frequent manual servicing may also benefit from selected through-hole mounting practices rather than an all-SMD layout.
Assembly choice
Best fit
Main trade-off
SMD
Compact products, short interconnects and automated volume assembly
Very small or hidden-joint packages may increase process and inspection demands
Through-hole
Large transformers, some high-power parts and mechanically stressed connections
Uses more board area and may require additional assembly operations
Mixed
Products combining dense electronics with large, heavy or stressed components
Requires careful process sequencing and may increase handling and tooling
How Do You Choose Among the Main Types of SMD Electronic Components?
Select the component technology from the required circuit behavior, then compare packages. A capacitance or resistance value alone does not describe bias behavior, pulse capability, noise, losses or stability.
Circuit task
Common SMD component
Selection focus
Biasing or current limiting
Thick-film or thin-film resistor
Tolerance, temperature coefficient, working voltage and pulse load
Decoupling or filtering
MLCC, film or electrolytic capacitor
Effective capacitance, voltage bias, ESR, ripple and polarity
Energy storage in switching power
Power inductor
Inductance under DC bias, saturation current, temperature-rise current, DCR and core loss
RF matching or filtering
RF inductor
Q factor, self-resonant frequency, impedance at the operating frequency and tolerance
Common-mode noise suppression
Common-mode choke
Common-mode impedance, differential-mode impact, rated current and insulation
Rectification or protection
Rectifier, Schottky, TVS or Zener diode
Reverse voltage, forward current, surge energy and leakage
Power switching
MOSFET or bipolar transistor
Voltage, current, safe operating area, conduction loss, switching loss and thermal path
Control, logic or signal processing
Integrated circuit
Supply range, I/O levels, required function, timing, pinout and package
Keep category boundaries clear. A ferrite bead, for example, may resemble a chip inductor but is normally selected by impedance-versus-frequency behavior and current rating rather than by inductance alone.
How Do You Determine the Required Electrical Ratings and Safety Margins?
Use worst-case conditions and documented derating. Electrical ratings for SMD electronic components must account for voltage, current, power, tolerance, temperature coefficient, frequency behavior, surge or pulse loading and expected aging. The correct margin depends on the component technology, duty cycle, ambient temperature, PCB cooling and reliability target.
For resistors, confirm both power and maximum working voltage. For MLCCs, evaluate effective capacitance after DC bias, tolerance and temperature effects. For inductors, distinguish saturation current from temperature-rise current. For semiconductors, calculate junction temperature from actual losses and the complete thermal path. Manufacturer datasheets and application notes should control these decisions; a universal derating percentage is rarely defensible across all SMD electronic components.
Worked example: Assume a resistor must drop 12 V at 10 mA. The required resistance is 12 V / 0.01 A = 1.2 kΩ, and the calculated dissipation is 12 V × 0.01 A = 0.12 W. If this project limits continuous dissipation to 50% of the rated power, the minimum rating is 0.24 W. A 0.25 W part only just clears that project gate, so its maximum working voltage and temperature derating still need to be checked; the next power rating may be the safer choice. The 50% limit is an example project rule, not a universal requirement.
How Do You Compare SMD Component Packages and Sizes?
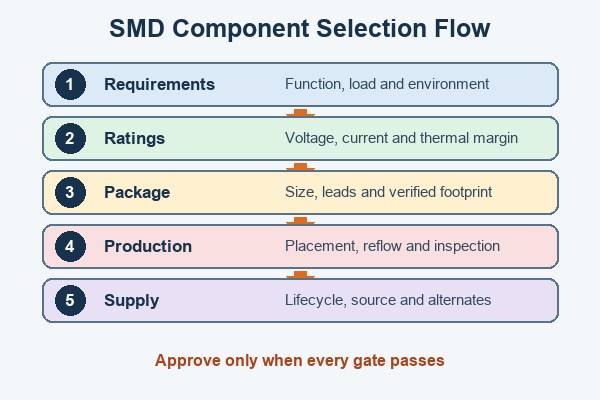
Eliminate every package that fails a mandatory requirement. Then choose the smallest option that passes all five steps. This SMD component size selection method prevents board-area savings from overriding electrical or production limits.
Check the electrical rating. Reject sizes that cannot handle the worst-case voltage, current, power or pulse load.
Check technology-specific behavior. Verify resistor working voltage, MLCC capacitance under DC bias, or semiconductor losses as applicable.
Check the thermal path. Reject power packages that cannot transfer the calculated heat through the available copper and airflow.
Check physical and assembly limits. Confirm height, terminal geometry, pad area, placement, inspection and rework access.
Choose between the passing sizes. Compare at least two exact part datasheets and select the smaller option only when it adds no unnecessary production risk.
Chip-passive codes such as 0402, 0603 and 0805 may use imperial notation, while metric codes describe different physical dimensions. Confirm the actual length and width in the datasheet rather than relying on the code alone. For SOT, SOIC, TSSOP, QFP, QFN, DFN and BGA families, compare body dimensions, terminal pitch, standoff, exposed-pad geometry and package height—not only the family name.
How Do You Choose the Right Lead, Termination and Package Configuration?
Balance density, heat transfer and joint visibility. The correct configuration must also fit the available assembly and inspection process. Apply these package-specific checks:
Chip terminations: Use them for most resistors, capacitors and other passives; verify the exact body size and end-metallization dimensions.
Gull-wing leads: Prefer SOIC, TSSOP or QFP when visible joints, probing and rework access matter, while allowing enough perimeter area.
J-leads: Use them when perimeter space must be reduced, but account for lower joint visibility and more difficult inspection.
QFN and DFN: Choose them for compact size, short electrical paths or exposed-pad heat transfer only when paste control and X-ray inspection are available.
BGA and CSP: Use area-array packages when interconnect density or routing demands them; confirm escape routing, X-ray capability and a practical rework strategy.
Final release checks: Verify the exact pinout, polarity or pin 1, exposed-pad function, pitch, terminal width, package height, thermal-pad geometry and manufacturer part-number suffix.
How Do You Verify That the SMD Package Matches the PCB Footprint?
Verify the exact orderable part number. For SMD electronic components, a matching package-family name does not prove that the PCB footprint is compatible. Use the latest controlled datasheet and an applicable land-pattern method such as IPC-7351, then complete these checks:
Package dimensions: Match terminal count, pitch, body size, terminal geometry, standoff and maximum component height.
Land pattern: Start from the manufacturer’s recommendation and adjust it only for a documented soldering or reliability need.
Pin mapping: Confirm pin numbering, electrical pinout, polarity and pin-1 orientation against the schematic symbol.
Thermal features: Check exposed-pad dimensions, paste segmentation, thermal vias and possible solder wicking.
Library release: Link the approved symbol, footprint, 3D body and manufacturer part number, then run a documented peer check.
How Do You Evaluate Thermal and Environmental Suitability?
Keep every worst-case exposure within documented limits. Thermal approval of SMD electronic components must include the required operating margin, not only the headline temperature rating. Review the following conditions separately:
Power loss: Calculate dissipation at maximum load, including duty cycle, switching loss, surge events and tolerance extremes where relevant.
Heat path: Include ambient temperature, nearby heat sources, PCB copper, thermal vias, airflow and the enclosure instead of relying on a package rating alone.
Thermal data: Use thermal-resistance values only when the datasheet test board and boundary conditions reasonably represent the intended layout.
Environmental exposure: Check humidity, vibration, mechanical shock, corrosive gases and temperature cycling against the product specification.
Required grade: Request the exact qualification and supporting documentation; temperature range alone does not establish automotive or industrial suitability.
Moisture sensitivity: Confirm MSL, floor life, dry storage and baking instructions from the component label and applicable J-STD-020/J-STD-033 controls.
How Do Placement, Soldering and Reflow Requirements Affect Component Selection?
Reject parts that fall outside the available process. Packaging, pickup surface, terminal geometry and temperature limits for SMD electronic components must suit the placement and soldering equipment. Confirm tape, tray or tube format, feeder compatibility, component dimensions, pickup area, centroid accuracy and rotation before release. Small passives, fine-pitch leads, bottom-terminated packages and high-thermal-mass parts each require a different process window.
Review stencil aperture design, paste type, PCB finish, component termination and reflow limitations together. Avoid assigning one universal reflow temperature to an entire BOM: the approved profile depends on solder paste, board construction, component temperature limits and thermal distribution across the assembly. Mixed package sizes can make it difficult to achieve sufficient wetting without overheating sensitive parts.
How Should Inspection and Testability Influence SMD Component Selection?
Select packages whose critical defects can be detected. Inspection plans for SMD electronic components should match joint visibility and the applicable acceptance criteria. AOI is effective for visible leads, polarity, presence and many solder-joint conditions, but it cannot directly view joints under QFN, LGA or BGA bodies. X-ray can reveal hidden-joint alignment, opens, bridges and void patterns. This limitation is also reflected in Analog Devices’ QFN assembly guidance, which describes transmission X-ray for post-reflow evaluation of concealed joints.
Package characteristic
Verification stage and method
Remaining blind spot
Visible chip or gull-wing joints
Before placement: SPI checks solder-paste deposits. After reflow: AOI or first-article inspection checks presence, polarity and visible joints.
Internal component damage or marginal electrical performance
Bottom-terminated QFN or LGA
Before placement: SPI checks paste deposits. After reflow: X-ray evaluates concealed joints; electrical or functional test is added where applicable.
Some interface defects may require process correlation or destructive analysis
BGA or CSP
Before placement: SPI checks paste deposits. After reflow: X-ray evaluates the ball array; functional or boundary-scan test is added where supported.
Intermittent defects may not appear in a static image
Design test points and programming access before layout is frozen. If a package eliminates probe access, the test strategy must compensate through connectors, boundary scan, built-in diagnostics or functional fixtures. A documented electronic product development testing plan should connect these access decisions to prototype, first-article and production acceptance tests.
How Do You Assess Component Availability, Lifecycle and Sourcing Risks?
Approve alternatives before a shortage occurs. Supply-risk reviews for SMD electronic components must use the exact part number; distributor stock alone does not make a part production-ready. Complete these checks:
Lifecycle status: Check active, NRND and end-of-life status, together with product-change and discontinuance notices.
Source coverage: Confirm availability through authorized channels and avoid dependence on one unverified source.
Order constraints: Review lead time, minimum order quantity, price breaks, packaging format and stock distribution for the planned build volume.
Traceability: Require the exact manufacturer part number, manufacturer identity, lot or date information and original packaging records as applicable.
Change control: Record approved alternates in the BOM and require documented review before any substitution reaches production.
Long-life planning: Monitor lead-time movement and manufacturer changes early enough to qualify a replacement or revise the design without stopping a build.
Which SMD Component Selection Mistakes Cause PCB Assembly Defects?
Many apparent soldering defects begin with a component, footprint or documentation decision. The defect still requires process evidence before assigning a root cause, but selection reviews can remove common contributors early.
Observed defect
Possible component, footprint or process contributors
Verification
Tombstoning or skew
Unbalanced pads, unequal termination wetting or unsuitable passive geometry
Check land pattern, paste deposits, placement and thermal balance
Bridging
Fine pitch, excessive paste or mismatched terminal geometry
Compare footprint, stencil data, SPI and reflow evidence
Insufficient solder or opens
Incorrect pad dimensions, poor coplanarity or paste-release limitations
Inspect paste transfer, package dimensions and joint formation
Voiding under thermal pad
Large exposed pad without suitable paste and via strategy
Review stencil segmentation, via design, profile and X-ray result
Cracked MLCC
Package placement in a high-flex board area or mechanical handling stress
Review layout location, depaneling, fasteners and failure analysis
Wrong or reversed part
Ambiguous BOM, markings, polarity or centroid rotation
Reconcile material-release records, kitting, assembly drawing and first article
How Do You Compare Candidate SMD Components and Make the Final Decision?
Reject any candidate that fails a mandatory requirement. Compare candidate SMD electronic components in a decision matrix, but do not let a low unit price compensate for an incompatible footprint, inadequate rating or unavailable inspection method. Score optional advantages only after all gates pass.
Decision gate
Required evidence
Owner
Circuit performance
Worst-case calculations, simulation or test plan and datasheet limits
Design review
Package and footprint
Controlled datasheet-to-library comparison
PCB design
Thermal and environmental fit
Thermal analysis and application requirements
Technical and quality review
Assembly and inspection
DFM review, process capability and inspection plan
Production review
Supply continuity
Lifecycle, authorized-source availability and approved alternates
Supply review
Final approval
Exact MPN, revision-controlled BOM and validation status
Cross-functional approval
For a new design, validate high-risk packages and substitutions through prototypes or a first-article build. Record the evidence behind the approved choice so later cost reductions or shortage substitutions do not erase the original technical constraints.
What Should Be Included in the Final BOM and PCB Assembly Package?
Release only exact, verifiable part data. The final package for SMD electronic components must state the approved part, placement information and finished-assembly verification requirements. Ambiguity transfers avoidable decisions into material preparation or production.
BOM: Include reference designators, quantity, description, exact manufacturer, MPN, package, lifecycle information and approved alternates.
PCB data: Supply Gerber or ODB++, fabrication information and the controlled board revision.
Placement data: Provide centroid coordinates, side, rotation and consistent design origins.
Assembly drawing: Show polarity, pin 1, special mounting, do-not-fit parts and process notes.
Process controls: Identify moisture-sensitive handling, baking, special soldering and cleanliness requirements.
Test requirements: Define inspection, programming, in-circuit or functional testing and acceptance criteria.
FAQs About Selecting SMD Electronic Components
Q1: How can you identify an unmarked SMD component on an assembled board?
A1: Match its reference designator to the controlled BOM and placement data, then verify the original reel or tray label when available. Appearance alone is not reliable enough to establish an exact orderable part number.
Q2: Can a zero-ohm SMD resistor be selected only by package size?
A2: No. Also check its current rating, maximum resistance, pulse capability and jumper function. A zero-ohm marking does not mean zero loss or unlimited current.
Q3: Can a ferrite bead replace an SMD inductor?
A3: Not as a direct substitute. A ferrite bead is normally specified by impedance over frequency and DC current, while an inductor is selected by inductance, bias behavior, saturation and loss.
Q4: Are all SMD capacitors polarized?
A4: No. Standard ceramic MLCCs are generally nonpolar, while aluminum electrolytic, tantalum and some specialty capacitors require correct orientation. Follow the exact datasheet and polarity marking rather than assuming from package shape.
Q5: When should a soft-termination MLCC be considered?
A5: Consider it where board flex, depaneling, vibration or thermal cycling creates a credible cracking risk. The termination option reduces mechanical stress but does not replace good component placement and board handling.
Q6: When is an anti-sulfur SMD resistor useful?
A6: It is useful where sulfur-bearing gases or materials may attack conventional silver-based terminations, such as some industrial, automotive or polluted environments. Confirm the required test condition and component qualification.
Q7: Must an IC exposed pad always be soldered to the PCB?
A7: Follow the exact datasheet. An exposed pad may provide heat transfer, electrical connection or both; leaving it unsoldered can cause overheating or functional failure when attachment is required.
Q8: Can a component top marking be used as the orderable part number?
A8: Usually not. Top marks may be abbreviated, shared across variants or combined with lot codes. Use the controlled BOM and packaging traceability to identify the exact part.
Q9: What should happen if a reel label differs from the BOM description?
A9: Stop material release and reconcile the exact manufacturer part number, package, value, lot and approved-alternate status. Do not place the part based only on a similar description.
Q10: Why can an MLCC make an audible buzzing or whining sound?
A10: Some ceramic dielectrics exhibit piezoelectric behavior, so changing voltage can make the capacitor and PCB vibrate. Capacitor construction, placement, board stiffness and the excitation waveform can all affect the noise.
Conclusion
A reliable component list is one that can be placed, soldered, inspected, tested and sourced without forcing last-minute changes. Finalize each selection at the exact manufacturer-part-number level and keep footprints, approved alternatives and assembly requirements under revision control.
Check package and production compatibility before release. Let EBest Circuit review whether your selected SMD electronic components, footprints and production requirements work together. Email your Gerber or ODB++ data, BOM with manufacturer part numbers and approved alternatives, build quantity, stackup, assembly drawings, programming method and test requirements to sales@bestpcbs.com. We will review package-to-footprint fit, assembly risks and inspection needs, then return practical feedback with a quotation for manufacturing quotation support.
To determine value of a shorted SMD capacitor, first confirm the failed component and preserve the evidence before removal. Because a hard-shorted capacitor can no longer reveal its original capacitance, recover the intended value from the schematic, BOM, boardview, a known-good board, a repeated circuit, or the IC manufacturer’s reference design.
Package size and board location narrow the possibilities but cannot identify capacitance by themselves. A visually identical part may have a different value, voltage rating, dielectric, tolerance, or function. The method below shows how to determine value of a shorted SMD capacitor without turning an uncertain guess into a second failure.
Can You Determine Value of a Shorted SMD Capacitor by Direct Measurement?
A hard-shorted capacitor cannot provide a valid capacitance reading. A capacitance or LCR meter applies a small test signal and observes the device’s response. When the dielectric has broken down and the terminals are connected by a low-resistance path, the instrument sees leakage or resistance instead of normal charge storage.
An in-circuit reading creates another problem: every component connected to the same net can affect the result. Semiconductor junctions, other capacitors, resistive loads, transformers, inductors, and internal IC paths may all sit between the probes. A continuity beep or a near-zero resistance reading therefore proves only that the rail has a low-resistance path. It does not identify the failed part or reveal the capacitor’s original value.
If the removed part no longer appears shorted after cooling, treat any capacitance reading as supporting evidence rather than proof. Heat and released board strain can temporarily change a marginal MLCC fault.
How Do You Confirm the SMD Capacitor Is Shorted Rather Than Another Parallel Component?
Confirm the faulty component by isolating the low-resistance rail and proving that the short disappears when the suspect part is removed. Treat the first meter reading as a symptom, not a verdict.
Step 1: Isolate and verify power removal. Disconnect the external supply, batteries, cables, and any backup source. Discharge stored energy by the product’s approved procedure, then confirm with a meter that the rail is no longer energized before using resistance or continuity mode. Do not work on mains, high-voltage, or large-capacitor sections without the specified discharge equipment and safety procedure.
Step 2: Inspect the rail before measuring. Under magnification, examine the suspect capacitor and nearby components for cracks, chipped corners, discoloration, corrosion, solder bridges, conductive debris, damaged vias, and disturbed joints. Record the reference designator and photograph the area before cleaning because visible evidence may help identify whether the capacitor failed from flex, impact, contamination, overheating, or an upstream electrical fault.
Step 3: Measure resistance in both probe polarities. Set the multimeter to resistance mode rather than relying only on the continuity buzzer. Measure between the rail and ground, reverse the probes, and allow several seconds for the reading to settle. A reading that starts low and rises may be normal capacitor charging; a stable near-zero reading in both directions is stronger evidence of a short, but it still does not identify which parallel component has failed.
Step 4: Compare equivalent points. Repeat the measurement with the same meter range, probe polarity, settling time, and power-off condition on a known-good board or an electrically identical channel. Confirm that the board revision, circuit option, IC population, and rail function match before using the comparison. Large differences help prioritize the suspect rail, while similar low readings may indicate that the circuit normally has low resistance.
Step 5: Localize the heat under controlled limits. Use current injection only after identifying the rail’s normal voltage and the safe limits of every connected device. Start below the rail voltage with a conservative current limit, monitor total current, and use a thermal camera, freeze spray, or another controlled indicator to locate the first component that warms. Stop immediately if an IC, trace, connector, or unknown part heats rapidly, and never increase voltage or current merely because the fault is difficult to find.
Step 6: Isolate and cross-check the suspect component. Remove the capacitor with a controlled rework process, or lift one terminal when the package and board permit it without pad damage. Measure the removed component and the two board pads separately after they cool. The diagnosis is confirmed when the capacitor remains low resistance while the board-side short disappears; if the pads remain shorted, the failed part is elsewhere on the shared rail and further isolation is required.
Do not apply an arbitrary bench-supply voltage to an unknown rail. The permitted voltage and current depend on the rail’s normal operating level, downstream IC limits, copper capacity, and the diagnostic method. If those limits are not known, trace the circuit or obtain design information before injection. A shorted IC, TVS diode, MOSFET, connector contamination, or solder bridge can heat near a capacitor and create a false conclusion.
What Should You Record Before Removing the Suspect SMD Capacitor?
Photograph and document the component before heat, cleaning, or removal changes the evidence. This record makes later value recovery and repair verification much more reliable.
Reference designator: Record the silkscreen identifier, such as C124, and any nearby IC or connector designators.
Board identity: Capture the PCB part number, assembly number, revision, variant, and serial or lot information when applicable.
Exact location: Take one close image and one wider image showing orientation, nearby parts, vias, and copper areas.
Package dimensions: Measure length and width with suitable magnification rather than estimating 0402, 0603, or 0805 by eye.
Electrical evidence: Record resistance to ground, probe polarity, meter range, rail name, and comparison readings from a good channel or board.
Physical condition: Note cracks, discoloration, lifted terminations, solder condition, contamination, or signs of flex damage.
Keep the removed part in a labeled container. Do not mix it with neighboring capacitors removed during fault isolation. If the component breaks during removal, retain the fragments because termination style and construction can still support identification.
How Can Schematics, BOMs and Boardviews Reveal the Original Capacitor Value?
The released schematic and BOM are normally the highest-confidence sources for the original value. Use the reference designator to connect the physical component to its circuit record, then verify that every document matches the exact board revision and assembly variant.
Evidence source
Confidence
What it can confirm
Main limitation
Released BOM and schematic
Highest
Capacitance, voltage, tolerance, dielectric, package, and approved MPN
Must match the manufactured revision and variant
Boardview or CAD database
High
Reference designator, net, footprint, placement, and circuit relationship
May omit purchasing specifications or approved alternates
Known-good identical board
High when controlled
Installed package and measurable out-of-circuit value
Must be the same revision, option, and population variant
Repeated circuit on the same board
Moderate to high
Likely matching value and function
Channels may use different compensation or option values
IC datasheet or reference design
Moderate
Expected value range and required capacitor characteristics
The production design may intentionally differ
Package size and location
Low
Plausible capacitance and voltage families
Cannot uniquely identify the original component
Start with the BOM’s manufacturer part number when available. A full MPN can reveal more than nominal capacitance: rated voltage, capacitance tolerance, dielectric class, package, temperature range, termination, and qualification grade. Check change notices, approved vendor lists, deviation records, and assembly option notes because the as-built part may differ from an early schematic value.
How Can a Donor Board or Repeated Circuit Help Identify the Capacitor Value?
A revision-matched donor board or an electrically identical repeated circuit can identify the missing value by providing a known-good capacitor in the same circuit position. Locate the matching reference designator or trace the same IC pins, power rail, ground return, and neighboring components. Before using it as evidence, confirm that the board revision, assembly variant, fitted IC, option resistors, and surrounding component population match the faulty circuit.
For a donor board, photograph the known-good component and record its package dimensions and location. If the repair procedure permits removal, measure the matching part out of circuit using the controlled LCR process described below. Use the result to identify the likely nominal capacitance, then confirm voltage rating, tolerance, dielectric, and other specifications from the donor BOM, schematic, approved part number, or manufacturer data.
A repeated circuit on the same PCB can be used in the same way when both channels are electrically equivalent. This is common in motor phases, communication ports, memory lanes, regulator phases, and repeated sensor inputs. Trace both capacitor pads and compare their connections rather than relying on visual symmetry. Similar-looking channels may use different values for compensation, startup timing, filtering, or EMC tuning, so the corresponding component becomes reliable evidence only after the net connections and circuit function match.
If removing a working donor component is not acceptable, use it only to confirm placement, package, and circuit relationship, then recover the exact value from its associated BOM or schematic. Do not treat an in-circuit capacitance reading as the final value because parallel capacitors, semiconductor paths, and other connected components can distort the measurement.
How Can Circuit Function, Package Size and Board Location Narrow the Value?
Circuit function can narrow the capacitor to a realistic value range; package size and board location provide supporting limits. Trace both pads and identify the connected pins, rail, and surrounding topology before selecting candidates.
Likely function
Location clue
Parameters that matter
Why guessing is risky
IC decoupling
Very close to a power pin and ground return
Capacitance under DC bias, voltage, dielectric, package, ESL
Too little effective capacitance can raise supply noise
Bulk rail support
Near a regulator, connector, or load cluster
Capacitance, voltage, ripple current, ESR, temperature
Wrong ESR or ripple capability can cause heating or instability
Switching regulator control
Connected to feedback, compensation, bootstrap, or soft-start pins
Exact value, tolerance, dielectric, leakage, voltage
A small change can alter loop response, timing, or switch stress
Signal coupling or filtering
In series with or shunting a signal path
Value, dielectric, tolerance, loss, voltage
Wrong value changes cutoff frequency or signal integrity
Safety or surge suppression
Across an isolation boundary, mains input, or protected interface
Safety class, impulse rating, technology, spacing
A same-size general capacitor may be unsafe
An 0603 footprint can hold many capacitance and voltage combinations. For Class II MLCCs such as X5R or X7R, the effective capacitance may fall substantially under applied DC voltage, especially in small packages. Package identification therefore cannot substitute for the application requirements or approved component data.
How Should You Measure a Matching SMD Capacitor With an LCR Meter?
Measure a known-good matching capacitor out of circuit with controlled test settings and proper fixture compensation. A basic capacitance reading is useful, but an LCR meter provides better control over frequency, signal level, and equivalent circuit assumptions.
Step 1: Prove that the comparison component is equivalent. Confirm that the donor board has the same PCB revision, assembly variant, IC version, option population, and circuit function as the faulty board. Match the reference designator when available; otherwise trace both capacitor terminals and verify that they connect to the same IC pins, rail, ground return, and surrounding network. Do not use a visually similar component from another channel until electrical equivalence is established.
Step 2: Remove the donor capacitor without changing its condition. Record its location and orientation, support the PCB, and use the approved temperature-controlled rework process for that package. Heat both terminations evenly and lift the part without twisting, pressing, or bending the board. Reject the test sample if the body chips, a termination separates, or excessive heat or mechanical force may have damaged the MLCC.
Step 3: Let the component stabilize and clean it. Place the removed part on a clean, nonconductive surface and allow it to return to room temperature before measurement. Remove flux with a compatible electronics cleaner and inspect the terminations for solder bridges, residue, cracks, or handling damage. Moisture, contamination, residual heat, and probe pressure can change a small-capacitance or high-impedance reading.
Step 4: Prepare and compensate the LCR fixture. Select an SMD tweezer fixture or short test fixture suitable for the component size, then perform the instrument’s open compensation with the contacts separated. Perform short compensation with the contacts joined in the same physical position used for measurement. Repeat compensation if the fixture position, cable, range, frequency, or test setup changes, and stop if the instrument reports an unstable or failed compensation.
Step 5: Use the correct measurement conditions. Select capacitance as the primary parameter and use the manufacturer’s specified test frequency, signal level, and equivalent-circuit mode when the MPN or capacitor family is known. If those conditions are unknown, measure at more than one appropriate frequency and record every setting instead of treating one default reading as authoritative. Keep contact pressure light and consistent, and remember that a zero-bias LCR reading does not reproduce the capacitance of a Class II MLCC under operating DC voltage.
Step 6: Confirm repeatability and interpret the result. Take at least three readings, removing and reseating the component between measurements; reverse it in the fixture when practical to expose contact-related variation. A credible result should stabilize and remain reasonably consistent after fixture uncertainty and component tolerance are considered. Use the measured value to identify the likely nominal capacitance, then verify voltage rating, dielectric, tolerance, package, DC-bias performance, temperature behavior, and aging from the BOM or manufacturer data. If readings drift widely or the original test conditions cannot be established, classify the value as unconfirmed rather than approving a replacement from that measurement alone.
How Do You Choose a Safe Replacement for a Shorted SMD Capacitor?
Match the electrical function and all critical ratings, not only the nominal capacitance. The safest replacement is the approved manufacturer part number or a documented alternate validated for the same circuit and assembly process.
Capacitance: Match the specified nominal value and ensure the effective value remains adequate under operating bias and temperature.
Voltage rating: Use a rating at least as high as the approved design value, while checking that a higher rating still fits and provides the required effective capacitance.
Dielectric: Preserve the required stability, loss, temperature range, and aging behavior. Do not replace C0G or NP0 timing parts with X5R or X7R merely because the nominal value matches.
Tolerance: Keep the specified tolerance where it affects filters, timing, compensation, sensing, or impedance.
Package and termination: Match the land pattern, component height, solderability, mechanical stress, and assembly profile.
Polarity: Confirm orientation for tantalum, aluminum, polymer, and other polarized chip capacitors. Most ceramic MLCCs are nonpolarized.
ESR and ripple capability: Check these for regulator outputs, bulk storage, pulsed loads, and circuits in which ESR contributes to stability.
Safety or qualification: Preserve required safety class, surge rating, temperature grade, and application qualification when those are part of the design.
When Is an Equivalent Capacitor Value Acceptable and When Is Guessing Unsafe?
Use an equivalent only when the circuit function is known and every critical replacement parameter stays within the approved design limits. Matching the footprint or obtaining one capacitance reading is not enough.
Situation
Decision
What must be confirmed
Approved MPN or documented alternate is available
Normally acceptable
Correct board revision, package, polarity, and approved sourcing status
Ordinary local decoupling with a fully understood rail
May be acceptable after verification
Nominal and effective capacitance, voltage rating, dielectric, tolerance, package, temperature range, and transient demand
Regulator input or output filtering
Requires circuit-level review
Effective capacitance under DC bias, ESR, ripple-current capability, regulator stability requirements, and startup behavior
Exact function plus tolerance, ESR, ESL, leakage, loss, voltage coefficient, and frequency behavior
High-voltage, surge, mains-connected, isolation, or safety-related position
Use only an approved specification
Safety class, rated and impulse voltage, capacitor technology, creepage or clearance implications, and applicable qualification
Original value or circuit function cannot be confirmed
Stop before installation
Obtain reliable documentation or complete a controlled engineering validation
Guessing is unsafe when the wrong capacitor could alter control-loop stability, timing, signal integrity, electrical safety, or component stress. In these positions, a candidate part must be supported by the schematic, BOM, approved manufacturer data, or a documented validation using simulation and instrumented prototype testing.
If the evidence remains incomplete, record the uncertainty and do not release the board as repaired. A temporary candidate used during controlled diagnosis is not automatically an approved production replacement.
How Do You Install and Verify the Replacement Without Causing Another Failure?
Repair is complete only after the root cause is addressed and the board passes controlled electrical and functional checks. A capacitor may have failed because of board flex, overvoltage, reverse polarity, excessive ripple, thermal stress, contamination, or damage elsewhere on the rail.
Step 1: Prepare and inspect the pads. Remove loose solder and flux with the approved rework materials, taking care not to scrape the solder mask or pull the copper. Under magnification, check that both pads remain flat and firmly attached, the connected vias are intact, and no copper has lifted. Stop the repair if a pad moves, a via barrel appears damaged, or the land no longer provides enough area for a reliable joint.
Step 2: Confirm that the short is gone. After the board and pads cool, measure resistance between the rail and ground using the same meter range, probe polarity, and settling time recorded before removal. The reading should change consistently with removal of the failed capacitor and should not remain at the previous stable near-zero value. If the rail is still shorted, do not install a replacement; continue isolating other capacitors, ICs, protection devices, solder bridges, and contaminated areas on the shared net.
Step 3: Position and solder the approved replacement. Verify the part number, package, capacitance, voltage rating, dielectric, and polarity before rework begins. Align the component centrally on both pads, use only enough solder to form controlled fillets, and follow the approved temperature profile or rework procedure. Heat both terminations evenly and avoid pressing, twisting, or cooling the MLCC abruptly because thermal and mechanical stress can crack the ceramic body.
Step 4: Inspect the completed joint. Under magnification, confirm that the component is flat, centered, and connected at both terminations with smooth, properly wetted joints. Look for bridges, solder balls, incomplete wetting, excessive solder, tombstoning, cracked corners, displaced neighboring parts, pad lifting, and conductive residue. Rework any visible defect before power is applied, and replace the capacitor if its body was chipped or stressed during installation.
Step 5: Apply power under controlled limits. When the product procedure permits, set a current-limited supply to the known rail or input voltage and begin with a conservative current limit based on the normal startup demand. Monitor input current, rail voltage, regulator behavior, and component temperature as power is introduced. Disconnect power immediately if current reaches the limit unexpectedly, the rail collapses, the replacement heats rapidly, smoke or odor appears, or another component becomes the first hot spot.
Step 6: Verify operation through realistic conditions. Check startup first, then confirm the repaired rail at idle, normal load, and the applicable transient or functional load. Observe rail voltage, ripple or noise when relevant, input current, temperature rise, and the function controlled by that circuit. Compare the results with the product specification or a known-good unit, and do not release a board that passes only at idle but fails during load changes or warm operation.
Step 7: Complete the repair record and release decision. After the board has operated and cooled, repeat the resistance and visual checks to confirm that the fault has not returned. Record the removed component, replacement MPN and lot, board revision, measured resistance, voltage, current, temperature observations, test conditions, and final functional result. Release the board only when every required check passes; otherwise record the unresolved symptom and return it for further diagnosis.
What Capacitor Details Should Be Recorded in the BOM After Repair?
Record enough information to reproduce the approved repair without repeating the investigation. A BOM entry that says only “0.1 µF capacitor” is incomplete for controlled production or long-term service.
Identification: Reference designator, internal part number, manufacturer, full MPN, and approved alternates.
Electrical specification: Nominal capacitance, tolerance, rated voltage, dielectric or capacitor technology, ESR or ripple requirement when applicable.
Mechanical specification: Package code, metric dimensions, height limit, termination type, and polarity marking when applicable.
Application controls: Temperature grade, safety class, qualification requirement, and any no-substitution note.
Update the controlled BOM and repair instruction rather than leaving the value only in a technician’s notes. If an alternate is approved, state the reason and the parameter comparison that supports equivalence. This prevents later procurement substitutions from silently changing circuit behavior.
FAQs About Determining the Value of a Shorted SMD Capacitor
Q1: Can a cracked MLCC fail intermittently instead of staying shorted?
A1: Yes, a crack can create an intermittent fault. Board flex, temperature change, vibration, or probe pressure may open and close a damaged internal electrode or termination. Record resistance while gently controlling temperature or mechanical stress, but do not flex a powered board unless the approved diagnostic procedure permits it.
Q2: Can a board be powered temporarily after a shorted decoupling capacitor is removed?
A2: Only as a controlled diagnostic step. Removing one capacitor may allow startup, but it can reduce local decoupling, increase supply noise, or disturb a high-speed return path. Use current-limited power, avoid full-load qualification, and install the approved replacement before release.
Q3: Should every capacitor in a parallel bank be replaced after one fails?
A3: Not automatically. Replace other parts only when evidence shows shared overstress, heat, contamination, age-related degradation, or an approved maintenance rule. MLCC banks do not require blanket replacement merely because one component cracked.
Q4: Can the color of an unmarked MLCC reveal its capacitance?
A4: No, body color is not a dependable value code. Ceramic formulation, coating, firing process, and manufacturer choices can produce similar colors across many capacitance and voltage combinations. Use the circuit location, documentation, or a verified comparison part instead.
Q5: Can soft-termination MLCCs reduce repeat cracking?
A5: They can improve resistance to board-flex stress. A flexible termination absorbs some strain between the ceramic body and PCB, but it does not correct poor component placement, excessive depaneling force, mounting-screw distortion, or an unsuitable footprint.
Q6: Can a tiny shorted MLCC damage a PCB trace or copper plane?
A6: Yes, package size does not limit fault current. A low-impedance supply can drive enough current through a small MLCC to overheat pads, vias, traces, or nearby laminate. Inspect the surrounding copper before fitting a replacement, especially when the failed part is discolored or charred.
Q7: Can a faulty MLCC behave like a resistor instead of a complete short?
A7: A damaged dielectric can create measurable leakage or resistive behavior. The reading may change with temperature, voltage, or time and may not trigger a continuity buzzer. Compare resistance under controlled conditions and isolate the part before deciding whether the rail itself is at fault.
Q8: Is a smaller MLCC package less likely to crack near a board edge or screw?
A8: Package size alone does not remove the risk. Smaller parts may experience less differential strain, but placement direction, distance from edges and fasteners, land geometry, PCB thickness, and assembly force also matter. Correct the mechanical cause before approving a size change.
Q9: Why can heating an MLCC change its measured capacitance?
A9: Heat can reset part of the aging behavior of Class II ceramic dielectrics. The measured value may rise after rework and then decrease as the component ages again. Allow the part to stabilize and compare it with the manufacturer’s specified test conditions rather than treating a hot reading as nominal.
Q10: Does a physically larger MLCC automatically make a safer replacement?
A10: No, a larger package is not automatically better. It may retain more capacitance under DC bias, but it can also change land compatibility, placement clearance, parasitic behavior, and board-flex stress. Approve the package change only after checking both electrical performance and assembly risk.
Conclusion
A failed shorted part cannot tell you what its capacitance used to be. To determine value of a shorted SMD capacitor, first prove that the component—not another device on the same rail—caused the fault. Recover the specification from revision-matched records or a verified comparison circuit, then check capacitance, voltage rating, dielectric, tolerance, package, ESR, polarity, and operating conditions before installing the replacement.
Need help turning a repair finding into a controlled production change? Send your Gerber or ODB++, NC drill files, BOM, board revision, stackup, quantity, assembly details, firmware or programming requirements, test plan, and required quality documentation to sales@bestpcbs.com. EBest Circuit can review the component substitution, assembly implications, and test requirements and then prepare a quotation.
PCBA manufacturing converts a bare printed circuit board into a functional electronic assembly. The process usually combines component sourcing, solder paste printing, automated placement, reflow soldering, through-hole assembly, inspection, programming, and electrical testing.
Component placement is only one part of the job. The larger risks often come from incorrect file revisions, unavailable parts, unsuitable footprints, weak test coverage, soldering defects, and unclear responsibility between the PCB fabricator and assembly provider.
A well-managed PCBA project therefore starts with complete production data and a clear definition of quality, testing, traceability, and delivery requirements.
What Is PCBA Manufacturing?
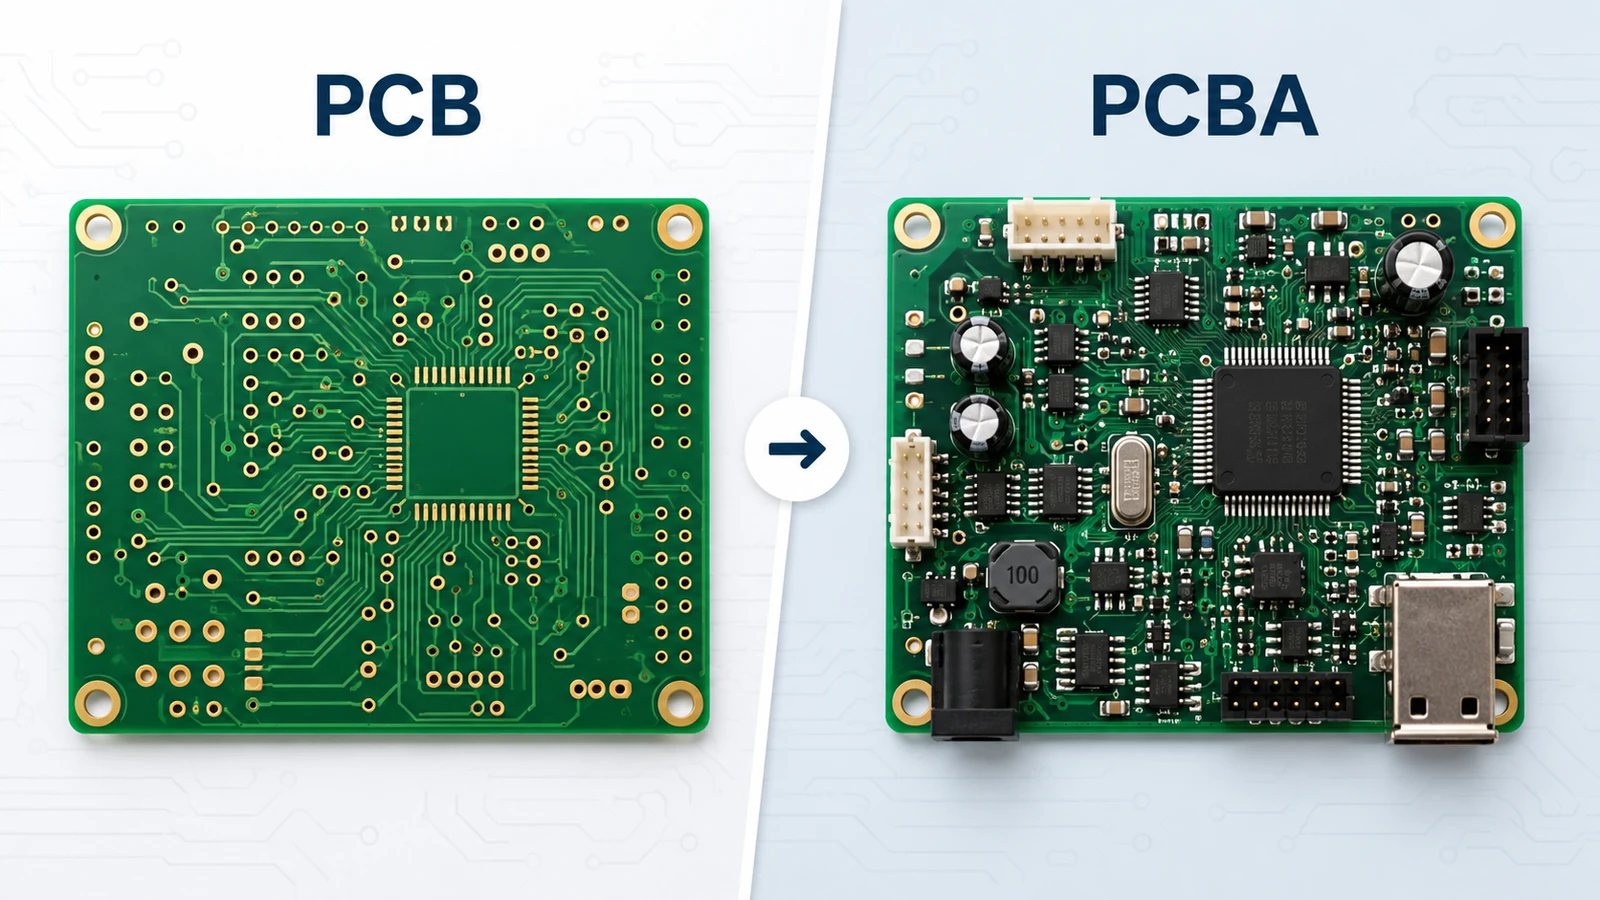
PCBA stands for printed circuit board assembly. PCBA manufacturing is the process of mounting electronic components onto a fabricated PCB and completing the soldering, inspection, and testing needed to make the assembly work.
A bare PCB contains copper traces, pads, plated holes, solder mask, and surface finish. It provides the electrical interconnection but does not perform the intended product function. Once resistors, capacitors, ICs, connectors, relays, sensors, and other parts are installed, the board becomes a PCBA.
Depending on the project scope, PCBA manufacturing may include:
Bare PCB fabrication
Electronic component sourcing
SMT assembly
Through-hole assembly
Manual soldering
Device programming
Electrical and functional testing
Conformal coating or potting
Cable installation
Final product or box-build assembly
The term “PCB population process” is sometimes used for component placement. In most technical and purchasing contexts, however, PCB assembly process or PCBA manufacturing process is clearer.
PCBA manufacturing is also different from PCB manufacturing. PCB manufacturing produces the unassembled board. PCBA manufacturing adds the parts, solder joints, firmware, and testing required to create a usable electronic assembly.
Why Choose EBest Circuit for PCBA Manufacturing?
EBest Circuit provides PCB fabrication and PCBA assembly through one coordinated manufacturing workflow. Its PCBA manufacturing services can reduce communication gaps between the bare board supplier, component sourcing team, and assembly factory.
One-Stop PCB and PCBA Support
EBest Circuit supports assemblies built on several PCB types, including:
Rigid PCB
Flex PCB
Rigid-flex PCB
HDI PCB
Aluminum PCB
RF and microwave PCB
Heavy copper PCB
Keeping PCB fabrication and assembly under one supplier is useful when board construction directly affects soldering. Surface finish, board warpage, pad geometry, copper distribution, panelization, and solder mask registration can all influence assembly yield.
Prototype and Production Support
Early-stage builds usually require more engineering communication than stable repeat orders. Footprint mismatches, missing polarity marks, unavailable components, and incomplete test instructions are common during prototype development.
EBest Circuit supports:
Engineering prototypes
Small-batch PCBA
New product introduction
First article builds
Pilot production
Repeat manufacturing
Volume production
Many PCB prototype projects do not require a rigid minimum order quantity. The practical minimum depends on PCB panelization, stencil cost, machine setup, component packaging, and testing requirements.
Assembly and Inspection Capabilities
Available PCBA manufacturing processes include SMT, through-hole, and mixed-technology assembly. Relevant capabilities include:
SMT placement accuracy up to ±25 μm
10-zone nitrogen reflow
Solder paste inspection
Automated optical inspection
X-ray inspection
Wave soldering
Selective soldering
In-circuit testing
Functional testing
MES-based production traceability
These processes support boards that combine fine-pitch ICs, BGAs, QFNs, connectors, relays, transformers, terminal blocks, and other mixed component types.
Quality Systems
EBest Circuit operates quality systems associated with industrial, medical, automotive, and aerospace electronics, including ISO9001, ISO13485, IATF16949, and AS9100D.
Certification should not replace a clear project specification. Customers should still define the required workmanship class, inspection criteria, traceability level, testing method, and documentation package.
For a quotation, customers can send Gerber files, a BOM, pick-and-place data, assembly drawings, quantity, and test requirements to sales@bestpcbs.com.
PCB Manufacturing vs PCBA Manufacturing: What Is the Difference?
PCB manufacturing creates the physical circuit board. PCBA manufacturing installs the electronic components and verifies that the completed assembly meets the required electrical and functional criteria.
Comparison Item
PCB Manufacturing
PCBA Manufacturing
Final output
Bare printed circuit board
Assembled electronic circuit board
Main inputs
Gerber or ODB++, drill files, stack-up, fabrication drawing
Bare PCB, BOM, pick-and-place file, assembly drawing
A combined PCB and PCBA supplier can simplify defect analysis when the root cause may involve pad design, board warpage, solder mask, surface finish, stencil design, or reflow conditions.
Separate sourcing can still make sense when the buyer has an approved component contract, an internal assembly line, or an established specialist supplier. The correct choice depends on responsibility, traceability, pricing transparency, and technical control rather than convenience alone.
What Files Are Required for PCBA Manufacturing?
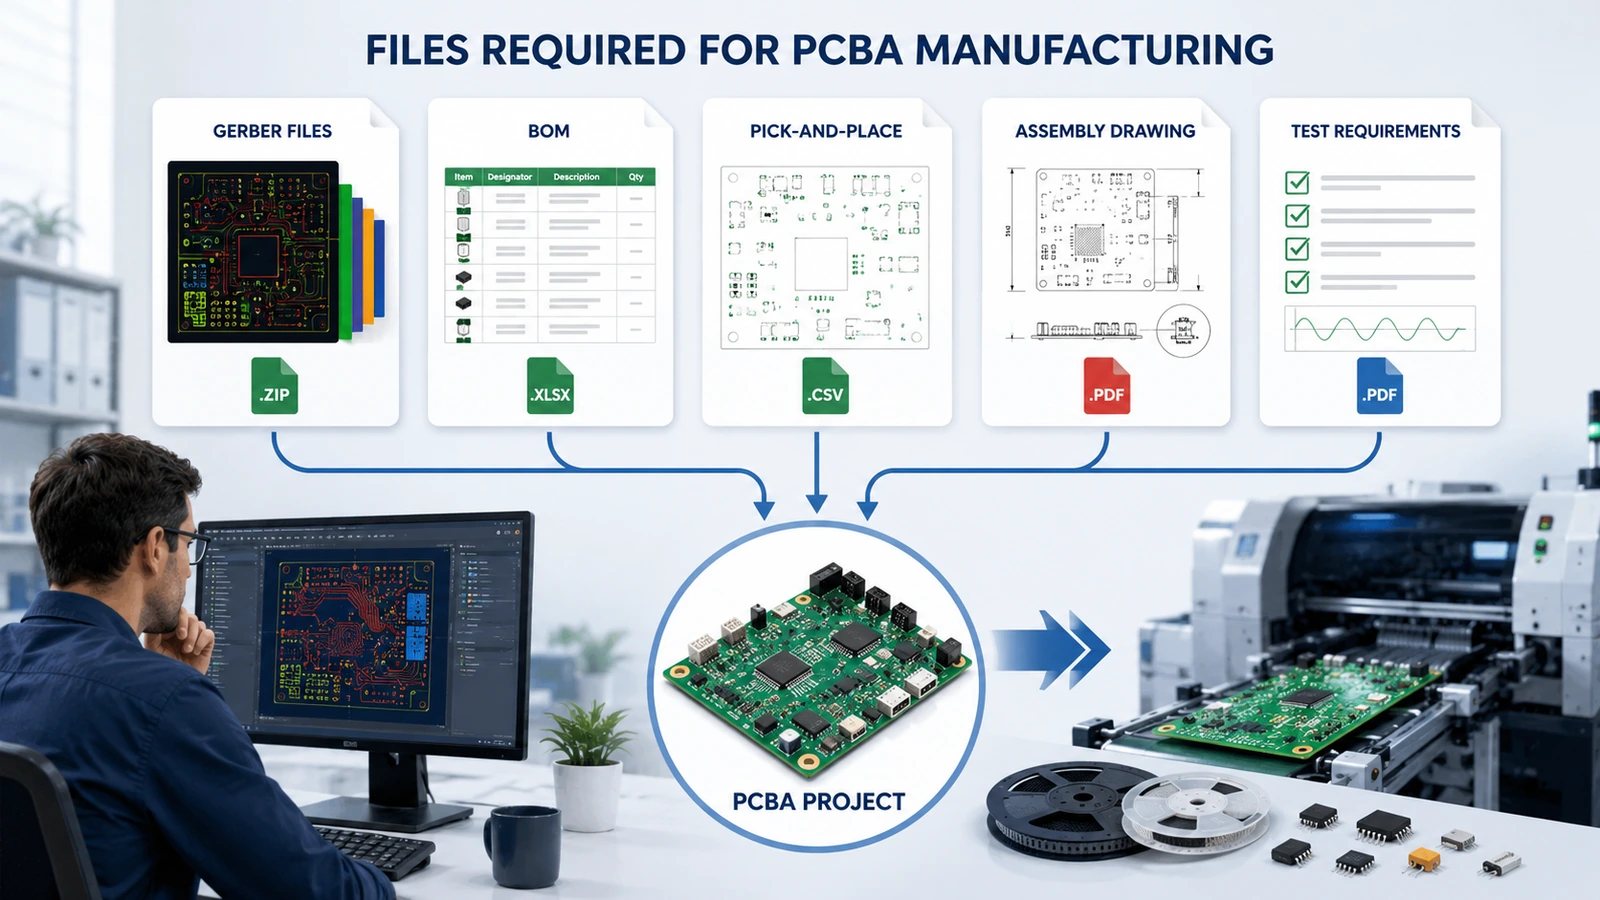
A complete file package allows the assembler to quote accurately, prepare machine programs, check component availability, and identify manufacturing risks before production.
File or Information
Main Purpose
Typical Problem
Gerber or ODB++
Defines PCB layers, pads, mask, and board outline
Missing data or incorrect revision
Bill of Materials
Identifies components and sourcing requirements
Incomplete part numbers or unclear specifications
Pick-and-place file
Provides component coordinates and rotation
Incorrect origin, rotation, or reference designator
Assembly drawing
Shows locations, polarity, and special assembly notes
Missing orientation or side identification
Fabrication drawing
Defines dimensions, stack-up, holes, and tolerances
Conflicts with Gerber data
Approved vendor list
Defines acceptable manufacturers or sources
No rule for alternative components
Programming file
Provides firmware or configuration data
Wrong firmware revision
Test procedure
Defines test steps and pass/fail limits
Incomplete measurement criteria
Golden sample
Provides a known-good functional reference
Sample does not match current revision
Order requirements
Defines quantity, delivery, packaging, and compliance
Unclear scope or deadline
The BOM should include complete manufacturer part numbers. A description such as “10 kΩ resistor” does not define package size, power rating, tolerance, voltage rating, temperature coefficient, or approved brand.
Component packaging also affects cost and manufacturability. Reels, trays, and tubes can feed automated equipment directly. Loose components or short cut strips may require manual preparation, repackaging, or placement.
All production documents should carry the same revision. A correct BOM combined with an outdated placement file can still produce incorrect assemblies.
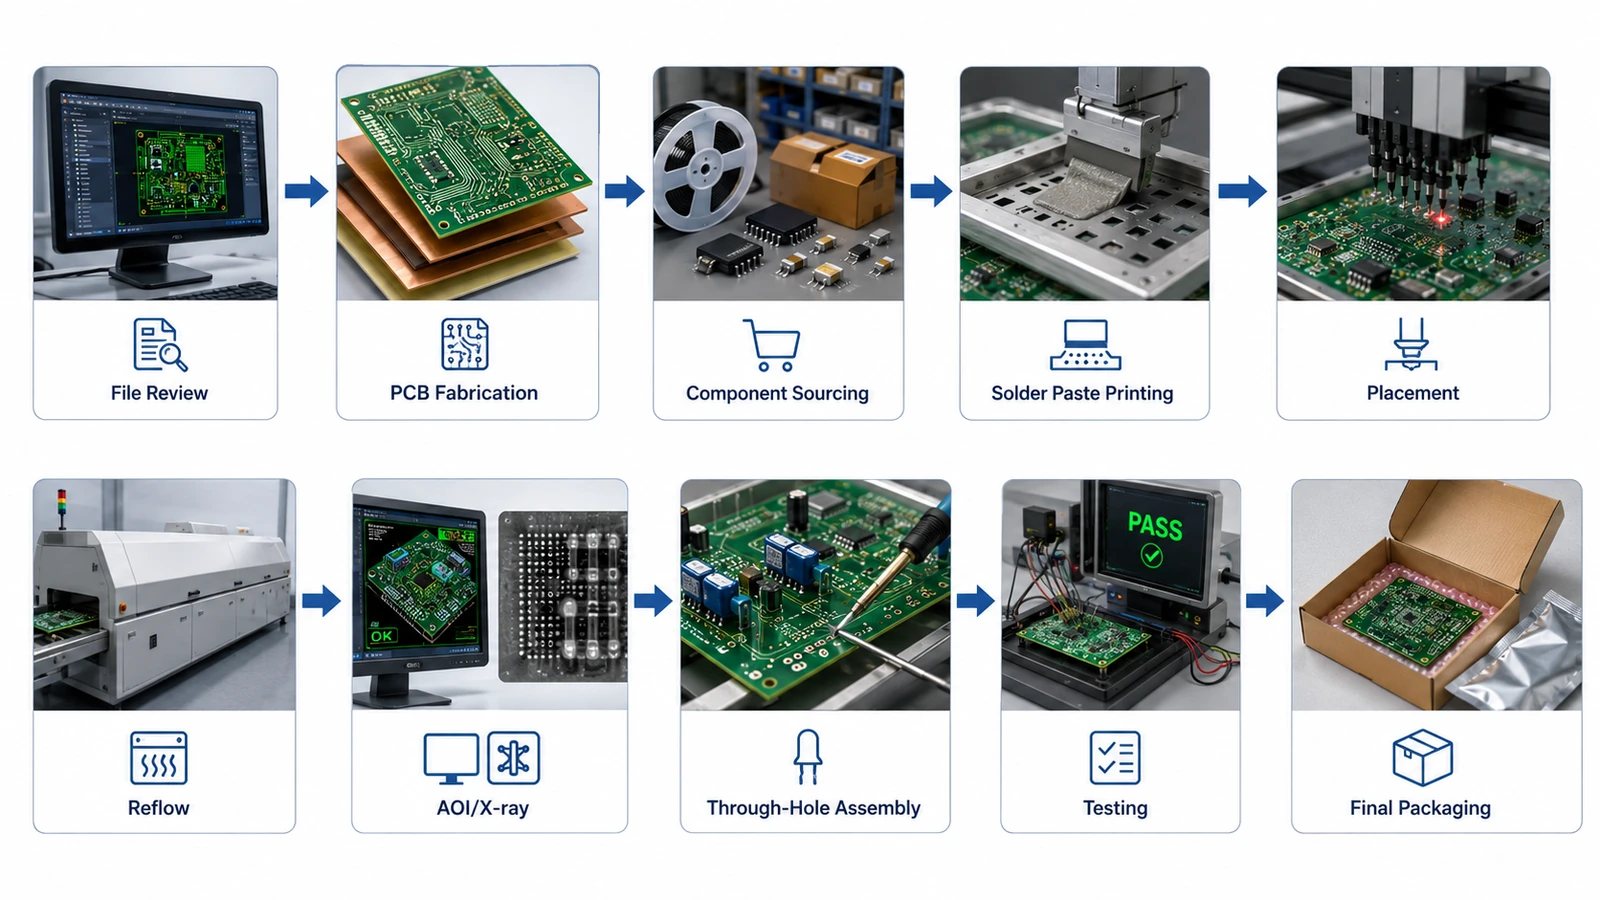
PCBA Manufacturing Process Flow: From DFM Review to Finished Assembly
The exact process varies by product, but most PCBA projects follow the same general manufacturing flow.
File Review and DFM Analysis
The manufacturer first checks the Gerber data, BOM, placement file, assembly drawing, and testing requirements.
The review should identify:
Component-to-footprint mismatches
Missing polarity information
Insufficient component clearance
Poor fiducial design
Unsuitable panelization
Inaccessible test points
Stencil aperture risks
Conflicting document revisions
Obsolete or long-lead components
DFM focuses on whether the PCB can be fabricated reliably. DFA addresses assembly risks. DFT checks whether the finished board can be tested efficiently.
PCB Fabrication
The bare PCB is produced according to the approved data. Surface finish, solder mask registration, pad dimensions, warpage, cleanliness, and copper balance can affect downstream soldering.
For example, excessive board warpage may reduce solder contact beneath large BGAs or bottom-terminated components. Poor solder mask definition can increase the risk of bridging on fine-pitch packages.
Component Sourcing
Components are purchased through approved manufacturers, authorized distributors, customer-nominated sources, or controlled inventory.
The sourcing review should confirm:
Manufacturer part number
Package type
Lifecycle status
Date-code requirement
Moisture sensitivity level
Minimum purchase quantity
Lead time
Approved alternatives
Lot traceability
One unavailable semiconductor can determine the project schedule even when PCB fabrication and assembly capacity are available.
Incoming Inspection
PCBs and components are checked before production. Inspection may include:
Part number and quantity verification
Packaging condition
Moisture sensitivity review
Component marking
PCB dimensions
Surface finish
Board warpage
Certificate and lot verification
Moisture-sensitive devices may require dry storage or baking before reflow.
Solder Paste Printing
A stencil deposits solder paste onto the SMT pads. Stencil thickness, aperture design, printing pressure, board support, paste condition, and separation speed affect the deposited volume.
Printing quality is especially important for 01005 components, fine-pitch leads, QFNs, and BGAs. Small changes in paste volume can create opens, bridging, or excessive voiding.
Solder Paste Inspection
SPI measures paste position, area, height, and volume before component placement.
It can identify:
Insufficient paste
Excess paste
Printing offset
Bridged deposits
Blocked apertures
Uneven transfer
Finding a paste problem before placement prevents defective boards from continuing through reflow.
Component Placement
Pick-and-place machines position components according to the centroid data.
Setup controls normally include:
Feeder verification
Package confirmation
Nozzle selection
Vision alignment
Polarity checking
Fiducial recognition
Program review
A first article board is often inspected before the full batch runs. This confirms component identity, position, rotation, and polarity.
Reflow Soldering
The populated board passes through a controlled heating profile with preheat, soak, reflow, and cooling stages.
The profile must account for:
Solder alloy
PCB material
Board thickness
Copper distribution
Component temperature limits
Surface finish
Thermal mass
Nitrogen reflow can reduce oxidation and improve wetting, but it is not required for every assembly. Its value depends on package geometry, alloy, finish, and the available process window.
AOI and X-Ray Inspection
AOI inspects visible component and soldering features, including:
Missing components
Placement shift
Incorrect polarity
Wrong component marking
Visible solder bridges
Exposed solder joint quality
X-ray is used for hidden connections such as:
BGA solder balls
QFN thermal pads
Bottom-terminated components
Hidden connector joints
Via-in-pad structures
Neither method confirms full electrical function. They should be combined with electrical or functional testing where product risk justifies it.
Through-Hole Assembly
Through-hole components may be inserted manually or automatically, then soldered by wave, selective, or controlled hand soldering.
The process choice depends on:
Number of through-hole joints
Bottom-side SMT components
Connector geometry
Component heat sensitivity
Board thermal mass
Production volume
Required barrel fill
Selective soldering is often suitable when only a few through-hole components are present or when nearby SMT parts cannot tolerate wave soldering.
Cleaning and Secondary Operations
Cleaning may be required by the flux chemistry, coating process, voltage level, leakage-current limits, or customer specification.
Secondary operations can include:
Device programming
Depanelization
Heat sink installation
Cable assembly
Conformal coating
Potting
Mechanical assembly
Serial-number labeling
“No-clean” flux does not mean the residue is acceptable for every application. High-voltage, high-impedance, medical, optical, and coated assemblies may require stricter cleanliness controls.
Electrical and Functional Testing
Testing may include continuity checks, flying probe testing, ICT, boundary scan, firmware verification, and functional testing.
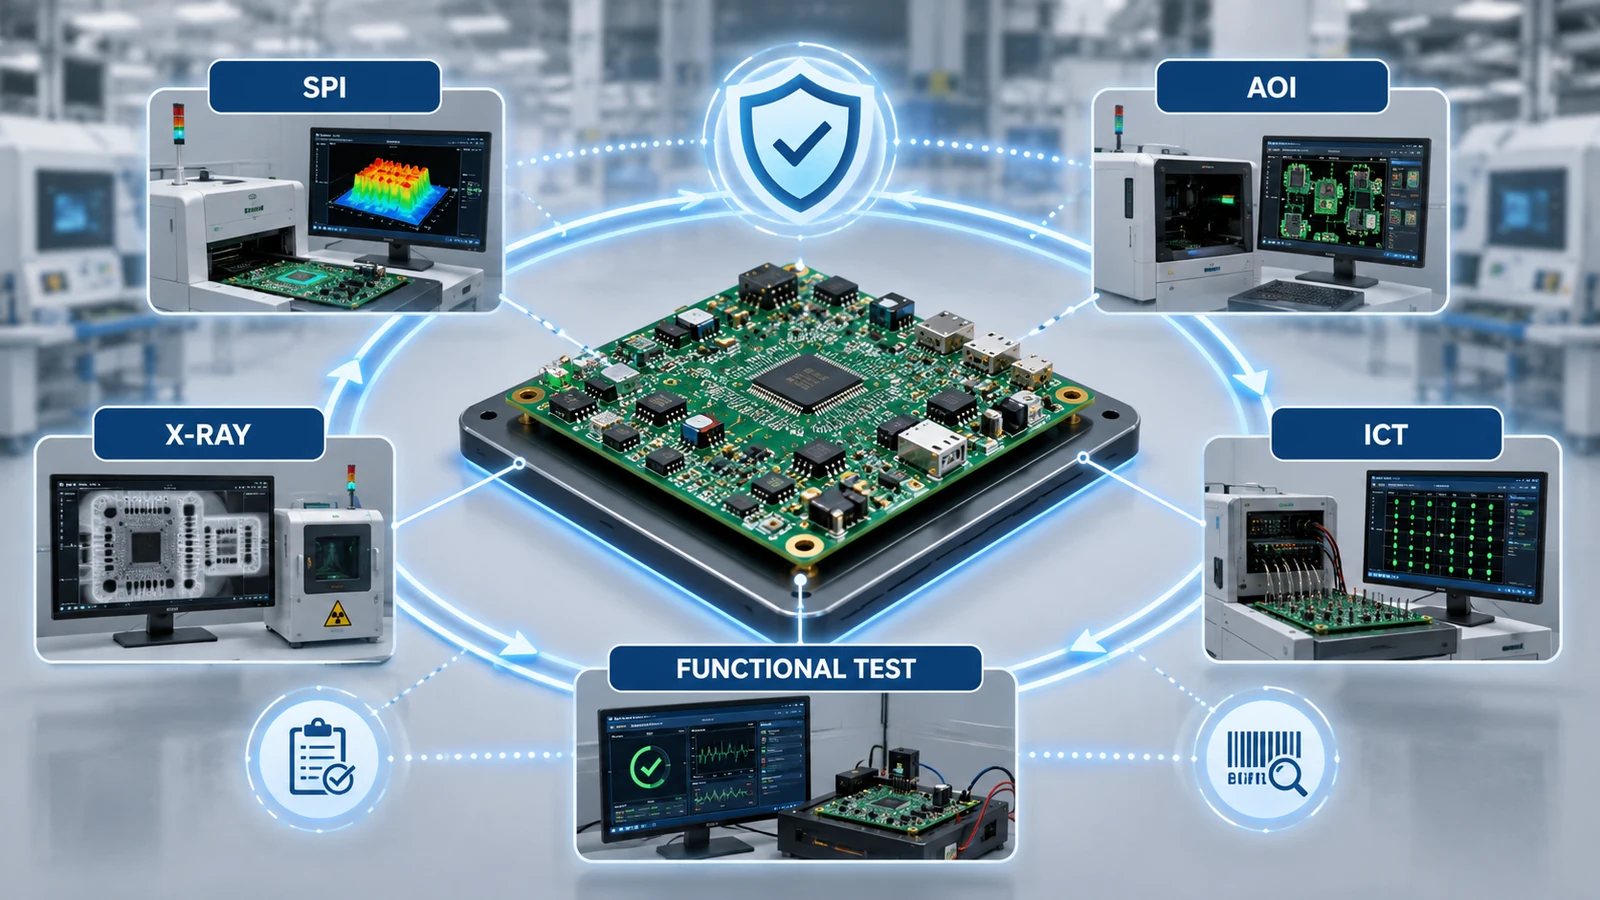
A practical PCB testing plan should address the most likely failure modes. Adding every available test increases cost without necessarily improving useful coverage.
Final Inspection and Packaging
Before shipment, the manufacturer verifies:
Visual condition
Labels and serial numbers
Firmware revision
Test records
Quantity
Packaging
Customer-specific documentation
Electrostatic-sensitive, moisture-sensitive, or mechanically fragile assemblies require suitable protective packaging.
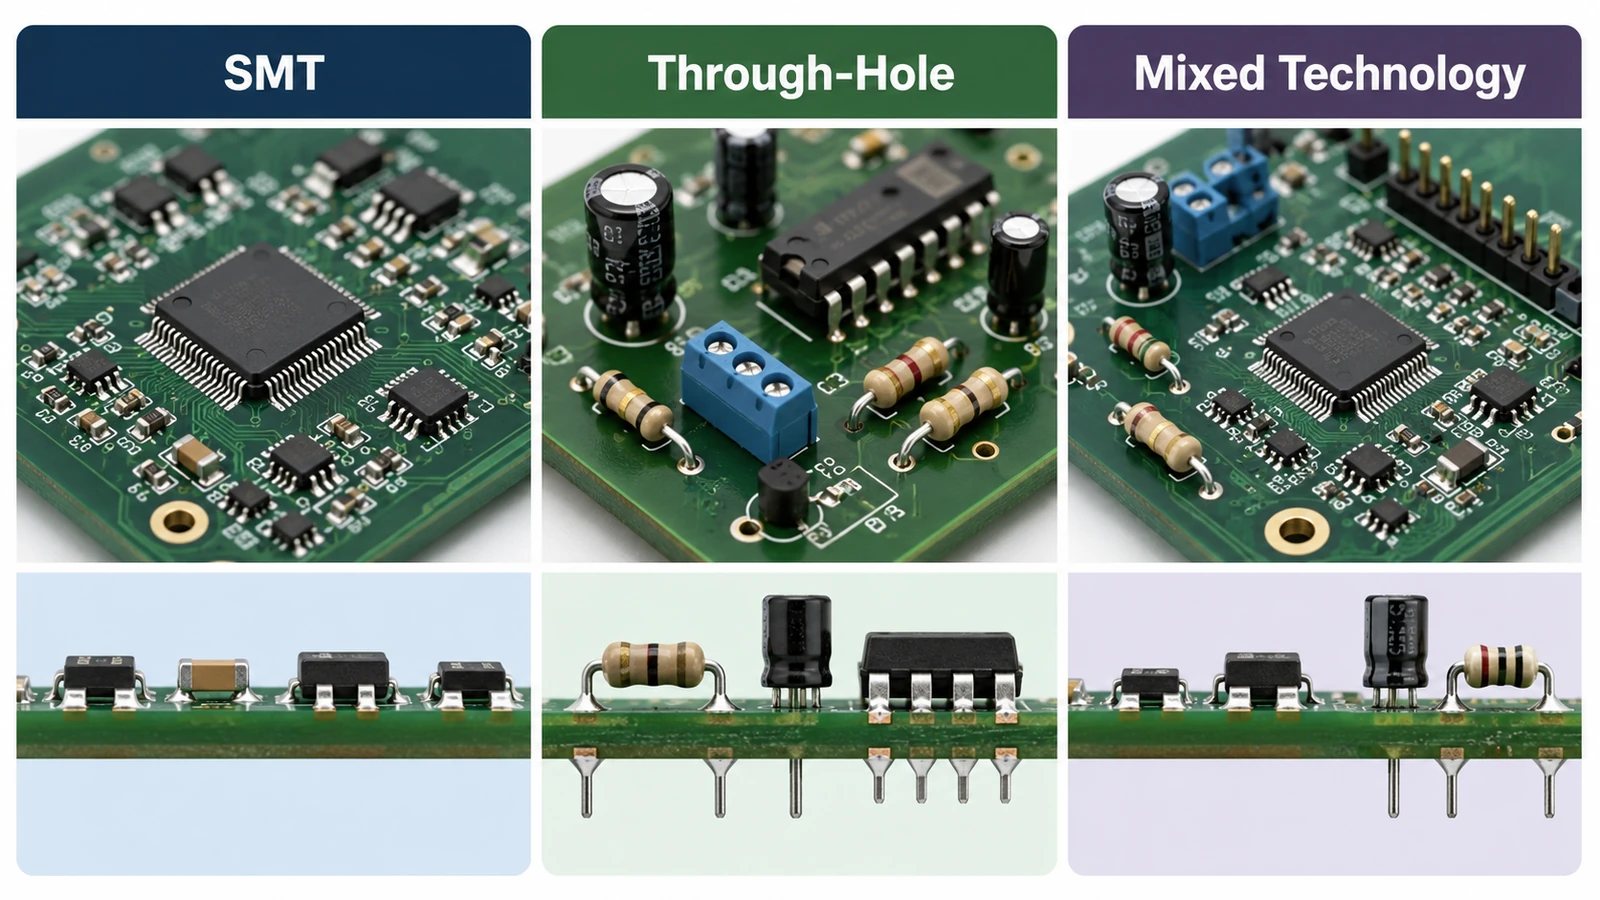
SMT, Through-Hole, and Mixed-Technology PCBA Manufacturing
The assembly method should match the component types, board density, mechanical loading, and expected production volume.
Factor
SMT Assembly
Through-Hole Assembly
Mixed-Technology Assembly
Mounting method
Components soldered to surface pads
Leads inserted through plated holes
Combines both methods
Assembly density
High
Lower
Medium to high
Automation
High
Moderate
Depends on product
Typical components
ICs, resistors, capacitors, semiconductors
Connectors, relays, transformers, large capacitors
Industrial, power, control, and communication boards
Mechanical retention
Suitable for most low-load parts
Strong lead-to-hole retention
Selected by component requirement
Soldering method
Reflow
Wave, selective, or hand soldering
Reflow plus secondary soldering
Main limitation
Some high-force parts need additional support
Uses more board area and labor
Requires more process stages
SMT suits compact products, dense layouts, and automated production. Components can be installed on both sides of the PCB, and the shorter interconnections also benefit many high-speed circuits.
Through-hole assembly remains useful for connectors, switches, relays, transformers, and parts exposed to repeated insertion force. It should not be used automatically for every large component. A correctly designed SMT joint may be sufficient when mechanical loading is limited.
Mixed assembly is common in industrial controls, power electronics, medical devices, automotive modules, and communication equipment. A typical sequence completes SMT reflow first, followed by through-hole insertion and selective soldering.
How Is Quality Controlled During PCBA Manufacturing?
Quality control combines incoming inspection, process monitoring, visual inspection, hidden-joint inspection, electrical testing, and traceability.
Method
Main Purpose
Typical Findings
Limitation
Incoming inspection
Verify PCBs and components
Wrong parts, damage, packaging issues
Does not confirm assembled performance
SPI
Measure solder paste
Low volume, excess paste, offset
Used before reflow
First article inspection
Confirm initial setup
Wrong value, position, or polarity
Covers the initial build only
AOI
Inspect visible features
Missing parts, shift, polarity, solder defects
Cannot fully inspect hidden joints
X-ray
Inspect hidden solder joints
BGA opens, bridges, voiding
Does not prove function
Flying probe
Test low-volume assemblies
Opens, shorts, selected component faults
Slower than dedicated ICT
ICT
Test networks and component values
Opens, shorts, wrong values
Requires test access and often a fixture
FCT
Verify product operation
Interface, firmware, signal, and power faults
Coverage depends on the test procedure
Burn-in
Screen selected early failures
Temperature- or time-related faults
Adds cost and production time
Process Control
Stable production depends on more than final inspection. Important controls include:
Solder paste storage and handling
Stencil condition
Printer setup verification
Feeder loading control
Reflow profile management
Moisture-sensitive component handling
Equipment calibration
First article approval
Controlled repair procedures
Traceability
The required traceability level should reflect product risk.
A basic prototype may need only a batch number and final test result. Automotive, medical, aerospace, and other high-reliability products may require records linking the finished PCBA to:
PCB production lot
Component lot or date code
Solder paste batch
Machine program
Inspection result
Test data
Repair history
Firmware revision
EBest Circuit uses MES-based records to support production and material traceability. Customers should define the required record retention, component-level tracking, and reporting format before production.
Acceptance Standards
IPC-A-610 is commonly used for electronic assembly acceptance, while J-STD-001 addresses soldered electrical and electronic assembly requirements.
The purchase specification should state the required class, revision, exceptions, and documentation. A general note such as “manufacture to IPC” is too broad for controlled production.
Common PCBA Manufacturing Defects and Their Causes
Many assembly defects have more than one possible cause. The process team should identify the origin rather than only repairing the visible symptom.
Defect
Likely Causes
Detection
Prevention
Solder bridge
Excess paste, misalignment, poor pad spacing
AOI, X-ray, electrical test
Optimize stencil, printing, and layout
Insufficient solder
Blocked aperture, poor transfer, weak wetting
SPI, AOI, X-ray
Maintain stencil and control paste release
Tombstoning
Uneven heating, unequal pad geometry, placement offset
AOI
Balance pads and thermal connections
Component shift
Placement error, paste movement, unstable reflow
AOI
Improve placement and profile control
Missing component
Feeder or pickup failure
AOI, first article inspection
Verify feeders and setup
Wrong component
BOM error, reel mix-up, weak material control
AOI, ICT, manual check
Use barcode and approved BOM control
Reversed polarity
Incorrect drawing or rotation data
AOI, FCT
Provide clear polarity and centroid data
Cold joint
Insufficient heat, contamination, oxidation
AOI, electrical test
Control profile, storage, and cleanliness
BGA open
Warpage, low paste, poor collapse
X-ray, ICT, FCT
Control coplanarity, paste, and profile
Excessive voiding
Pad design, volatiles, thermal profile
X-ray
Adjust stencil pattern, paste, and reflow
Solder balling
Excess paste, moisture, poor preheat
AOI
Control paste volume and component condition
Lifted pad
Excessive rework heat or mechanical force
Visual inspection
Limit rework cycles and use controlled tools
Some problems originate in the PCB design rather than the production line. Incorrect footprints, missing solder mask dams, uneven thermal connections, poor fiducial placement, and inaccessible test points may require a design revision.
What Determines PCBA Manufacturing Cost and Lead Time?
A PCBA quotation normally includes the bare board, components, assembly, tooling, testing, and any secondary operations.
Cost or Schedule Factor
Cost Effect
Lead-Time Effect
PCB complexity
Special materials and structures raise fabrication cost
More manufacturing stages are required
BOM value
Semiconductors and connectors may dominate total cost
Long-lead parts can delay production
Order quantity
Setup cost is spread across more units
Larger orders require more line capacity
Component packaging
Reels and trays support automation
Loose parts need additional preparation
Fine-pitch or BGA parts
Tighter control and X-ray may be required
Inspection adds processing time
Through-hole content
More insertion and soldering labor
Manual work reduces throughput
Double-sided SMT
Requires another print, placement, and reflow cycle
Adds an assembly stage
ICT fixture
Adds tooling cost
Fixture development requires time
Functional testing
Depends on equipment and cycle time
Long tests can limit daily output
Programming
Adds handling and verification
Firmware must be ready before release
Coating or potting
Adds material, masking, curing, and inspection
Curing extends the schedule
Box build
Adds mechanical parts and labor
Requires more materials and workstations
Component availability frequently has the greatest influence on total lead time. Assembly may require only a few days after all materials arrive, while one unavailable IC can delay the complete project.
A quotation request should include:
Complete manufacturer part numbers
Rules for alternative components
Prototype and production quantities
Expected repeat demand
Test requirements
Programming files
Coating or potting requirements
Packaging instructions
Target delivery date
EBest Circuit can quote PCB fabrication, component sourcing, assembly, inspection, and testing as one package. Standard production may take approximately 3–5 days for suitable projects after materials and approved engineering data are available.
Complex PCB structures, unavailable components, custom fixtures, conformal coating, potting, or box build require additional time. An expedited assembly schedule should therefore be confirmed against actual material status rather than assembly capacity alone.
Prototype, Low-Volume, and Mass-Production PCBA Manufacturing
The manufacturing objective changes as the project moves from prototype to volume production.
Stage
Main Objective
Recommended Controls
Common Mistake
Prototype
Verify design and function
DFM review, flexible sourcing, first article inspection
Expecting volume pricing
Low-volume build
Stabilize the process
Yield review, BOM confirmation, test refinement
Ignoring setup and test cost
Pilot run
Confirm production readiness
Fixture validation, work instructions, traceability
Scaling before defects are closed
Mass production
Maintain consistency and cost
SPC, sourcing control, capacity planning
Changing parts without approval
Repeat order
Reproduce an approved build
Revision control and retained programs
Assuming stock and pricing remain unchanged
Prototype Builds
A prototype should identify:
Footprint errors
Mechanical interference
Incorrect polarity
Power or signal problems
Firmware issues
Test-access limitations
Assembly risks
Component availability problems
A prototype that powers on is not automatically ready for volume production. The design must also be repeatable, testable, and supportable by the supply chain.
Low-Volume and Pilot Production
Low-volume builds help confirm whether the assembly process is stable. This stage is suitable for refining the reflow profile, validating the test procedure, checking yield, and approving alternative components.
Pilot production should use processes close to the intended mass-production method. Excessive manual adjustment can hide problems that will return at higher volume.
Mass Production
Volume manufacturing requires:
Released and controlled files
Approved sourcing channels
Defined alternative-part rules
Stable machine programs
Documented inspection criteria
Validated test fixtures
Repair and deviation procedures
Batch traceability
Capacity planning
EBest Circuit supports projects from engineering prototypes through repeat production. Keeping PCB data, component sourcing, assembly records, and engineering changes within one workflow can simplify scaling.
How to Choose a PCBA Contract Manufacturer?
A suitable contract manufacturer should match the product’s technical risk, volume, industry requirements, and expected lifecycle.
Confirm the Scope
Check whether the supplier provides:
PCB fabrication
Component sourcing
SMT assembly
Through-hole assembly
Programming
Electrical testing
Functional testing
Coating or potting
Box build
Failure analysis
Some manufacturers outsource part of the work. That is not automatically a problem, but ownership of quality, traceability, and corrective action should be clear.
Match the Equipment to the Product
Confirm that the factory can process the actual component and PCB features in the design, such as:
Fine-pitch ICs
BGAs
QFNs and LGAs
01005 components
Double-sided SMT
Large bottom-terminated packages
Heavy connectors
Press-fit components
Flex or rigid-flex assemblies
High-current terminals
A general statement such as “we support SMT” does not confirm suitability for every package or board structure.
Review Test Coverage
The inspection and test plan should match the product risk.
Examples include:
SPI for fine-pitch paste printing
X-ray for BGA and QFN joints
ICT for assemblies with suitable test access
Flying probe for prototypes or low-volume orders
FCT for firmware-controlled or interface-dependent products
Ask what the supplier means by “100% tested.” In some quotations, this may refer only to visual inspection or a simple power-on check.
Examine Component-Sourcing Controls
The manufacturer should explain:
Approved sourcing channels
Counterfeit-risk controls
Alternative-part approval
Date-code requirements
Moisture-sensitive storage
Customer-supplied material handling
Excess-component ownership
Lot traceability
A low assembly price may be offset by unclear component sources, unnecessary minimum purchases, or weak handling of unused stock.
Evaluate Engineering Communication
Useful indicators include:
Specific DFM comments
Clear BOM questions
Controlled file revisions
Written substitution approval
Traceable engineering changes
Defined deviation procedures
Named technical contacts
Fast communication is useful, but accurate engineering communication prevents more expensive production errors.
Compare Quotations on the Same Scope
A clear quotation should separate:
PCB cost
Component cost
Assembly cost
Stencil and tooling
Programming
Testing
Coating or potting
Box-build work
Freight
Excess material
Two quotations are not directly comparable when one includes functional testing and the other includes only visual inspection.
FAQ
1. What does PCBA manufacturing mean?
PCBA manufacturing is the process of mounting electronic components onto a bare PCB and completing the soldering, inspection, programming, and testing required to create a functional assembly.
2. What is the difference between PCB and PCBA manufacturing?
PCB manufacturing produces the unassembled circuit board. PCBA manufacturing installs and solders the components and may also include programming, testing, coating, and final assembly.
3. What are the main steps in the PCBA manufacturing process?
The process usually includes file review, PCB fabrication, component sourcing, incoming inspection, solder paste printing, SPI, placement, reflow, AOI or X-ray, through-hole assembly, testing, final inspection, and packaging.
4. What files are required for PCBA manufacturing?
Most projects need Gerber or ODB++ data, a BOM, pick-and-place file, assembly drawing, order quantity, and test requirements. Programming files and a golden sample may also be required.
5. What is SMT in PCBA manufacturing?
SMT, or surface-mount technology, places components directly onto pads on the PCB surface. It supports compact layouts, high component density, and automated production.
6. What is the difference between SMT and through-hole assembly?
SMT components are soldered to surface pads. Through-hole leads pass through plated holes before soldering. Through-hole assembly is commonly used for connectors, relays, transformers, and mechanically loaded parts.
7. How long does PCBA manufacturing take?
Assembly may take several days after all PCBs, components, files, and test instructions are ready. The total lead time depends mainly on component availability, PCB complexity, quantity, testing, and secondary processes.
8. What determines PCBA manufacturing cost?
The main factors are PCB complexity, BOM value, quantity, setup, component packaging, fine-pitch parts, through-hole labor, inspection, programming, testing, tooling, coating, and box build.
9. What is the difference between SPI, AOI, X-ray, ICT, and FCT?
SPI checks solder paste. AOI checks visible components and solder joints. X-ray examines hidden joints. ICT tests electrical networks and component values. FCT verifies actual product operation.
10. Can one supplier handle both PCB manufacturing and PCBA assembly?
Yes. A one-stop supplier can fabricate the board, source components, assemble the PCBA, test it, and complete secondary processes. The supplier’s actual capabilities and responsibility boundaries should still be verified.
11. Does EBest Circuit support prototypes and small-batch PCBA?
Yes. EBest Circuit supports engineering prototypes, small-batch production, pilot runs, repeat orders, and volume manufacturing.
12. What PCBA testing services does EBest Circuit provide?
Available services include SPI, AOI, X-ray, ICT, functional testing, and customer-defined test procedures. The suitable combination depends on package type, test access, quantity, and product risk.
13. Can EBest Circuit source electronic components?
Yes. EBest Circuit can source components as part of turnkey or partial-turnkey PCBA manufacturing. Customers should provide complete part numbers and state whether alternatives are permitted.
14. What certifications does EBest Circuit have?
EBest Circuit operates quality systems that include ISO9001, ISO13485, IATF16949, and AS9100D. Customers should still define the exact acceptance, documentation, and traceability requirements for the project.
15. How can I request a PCBA manufacturing quotation?
Send the Gerber files, BOM, pick-and-place data, assembly drawings, quantity, test requirements, and target delivery date to sales@bestpcbs.com. Include firmware, coating, packaging, and box-build requirements where applicable.
A DPDT relay diagram helps engineers understand how a double pole double throw relay switches two independent circuits at the same time. It is commonly used for polarity reversal, motor direction control, signal switching, power path selection, and industrial control boards.
For PCB and PCBA projects, however, understanding the diagram is only the first step. The relay must also match the PCB footprint, coil voltage, contact rating, creepage and clearance, soldering process, thermal requirement, and test method. EBest Circuit (Best Technology) supports PCB fabrication, BOM review, component sourcing, SMT and through-hole assembly, DFM checking, and functional test coordination for relay control PCB and PCBA projects. If you are preparing a relay board, control PCB, or assembled PCBA, please send your Gerber files, BOM, drawings, datasheets, and assembly notes to sales@bestpcbs.com for review before production.
How to Read a DPDT Relay Diagram
A DPDT relay means Double Pole Double Throw. “Double pole” means the relay controls two separate circuits. “Double throw” means each circuit can switch between two output paths.
A basic DPDT relay diagram usually includes:
Part
Meaning
Coil
Electromagnetic control side
COM
Common terminal
NO
Normally open contact
NC
Normally closed contact
Pole 1
First switching circuit
Pole 2
Second switching circuit
When the coil is not energized, each COM terminal usually connects to its NC terminal. When the coil is energized, each COM terminal switches to its NO terminal.
This is why a DPDT relay is often described as two SPDT switches controlled by one coil. But in real PCB design and PCBA production, you should still treat the relay as one physical component with one datasheet, one footprint, one coil rating, and one contact rating.
The most important rule is simple: do not rely on a generic DPDT relay diagram alone. Always check the relay datasheet and pinout. Different relay models may use different pin numbering and package layouts.
DPDT Relay Symbol and Pinout Explained
A DPDT relay symbol usually shows two switch sections and one coil. The coil controls both contact groups at the same time.
In many diagrams, you will see two groups like this:
COM1, NO1, NC1
COM2, NO2, NC2
Coil A, Coil B
The symbol explains the electrical function. The pinout explains the physical terminal arrangement. These two are related, but they are not the same thing.
For PCB projects, this difference matters. A schematic symbol may look correct, but the PCB footprint may still be wrong if the pin mapping does not match the actual relay datasheet.
Before manufacturing, the engineering file should confirm:
Coil pins
Contact pins
COM, NO, and NC mapping
Pin pitch
Relay body size
Through-hole or surface-mount package
Clearance between coil side and contact side
Mechanical height and enclosure fit
A wrong relay pinout can cause a prototype to fail even when the circuit idea is correct.
8 Pin DPDT Relay Wiring Diagram
An 8 pin DPDT relay wiring diagram is common because many DPDT relays use 2 coil pins and 6 contact pins.
A typical 8 pin DPDT relay includes:
Pin Group
Function
2 pins
Coil
2 pins
COM terminals
2 pins
NO terminals
2 pins
NC terminals
However, the exact pin numbers depend on the relay model. Some relays place coil pins on one side. Some use a symmetrical layout. Some socket-mounted relays follow a different numbering system from PCB-mounted relays.
For PCB and PCBA work, the 8 pin diagram should be checked against:
Relay datasheet
PCB footprint
Silkscreen marking
Drill hole size
Pad size
Contact current requirement
Relay socket requirement, if used
Assembly orientation
If the board is already designed, EBest Circuit can help review whether the relay footprint, hole size, pad size, and assembly notes are clear enough for production. We do not change the circuit function without customer approval, but we can help catch manufacturability risks before the board is built.
DPDT Relay Wiring Diagram for DC Circuits
A DPDT relay wiring diagram for DC circuits is often used for polarity reversal or motor direction control. By crossing the contact connections correctly, the relay can reverse the polarity applied to a DC motor or load.
This is one reason the related keyword dc relay wiring diagram dpdt has strong search demand. Many users are trying to understand how a relay changes current direction.
For PCB projects, DC relay circuits need more than a correct diagram. The board should also consider:
Load current
Contact rating
Coil voltage
Coil drive transistor or MOSFET
Flyback diode or suppression circuit
Trace width for load current
Copper thickness
Heat rise
Terminal block or connector rating
Isolation between control and load circuits
If the relay drives an inductive load such as a motor, solenoid, or valve, suppression components may be needed to protect the driver circuit and reduce electrical noise. The exact circuit choice belongs to the customer’s design team, but the PCB manufacturer should check whether the layout, spacing, copper, and assembly files can support the requirement.
SPDT vs DPDT Relay Diagram Differences
An SPDT relay, also called a single pole double throw relay, has one common terminal switching between one NO and one NC contact. A DPDT relay has two such switching groups controlled together. When reading the schematic, it also helps to recognize the switch SPDT symbol, because a DPDT relay diagram is essentially two SPDT-style switching sections controlled by one coil.
Relay Type
Contact Structure
Typical Use
SPDT
1 COM, 1 NO, 1 NC
One circuit changes state
DPDT
2 COM, 2 NO, 2 NC
Two circuits switch together
It is also important not to confuse DPDT with other pole-and-throw structures. For example, a single throw double pole switch PCB uses a different contact logic from a DPDT relay, because it switches two poles in only one throw position instead of switching each pole between two throws.
A DPDT relay is useful when two paths need to change at the same time. Examples include:
Reversing DC motor polarity
Switching two signal lines
Selecting between two power paths
Isolating two control channels
Changing load connections in pairs
A DPDT relay is not automatically better than an SPDT relay. It is larger, may cost more, and may require more PCB space. If only one circuit needs switching, SPDT may be enough. If two circuits must switch together, DPDT becomes useful.
For PCB layout review, the practical question is not only “SPDT or DPDT?” It is whether the selected relay matches the circuit current, voltage, footprint, board space, and assembly method.
Double Pole Double Throw Relay Diagram Applications
A double pole double throw relay diagram is especially useful when the switching logic is easier to understand visually than through text.
Common applications include:
DC motor forward and reverse control
Battery polarity switching
Audio or signal path selection
Industrial control modules
Test equipment switching
Automation relay boards
Safety interlock circuits
Power source selection
For PCBA projects, these applications often involve connectors, terminal blocks, high-current traces, mixed signal paths, or through-hole relay assembly.
Manufacturing review should pay attention to:
Relay body clearance
Connector location
Terminal current rating
Copper width for load paths
Solder joint strength
Mechanical stress during plugging and unplugging
Board thickness and mounting method
Test points for relay output verification
A relay circuit may look simple, but the assembled board must survive real switching, load current, heat, vibration, and repeated operation.
DPDT Relay PCB Layout Checks Before Manufacturing
For a DPDT relay board, PCB layout manufacturability should be reviewed before production starts.
Important checks include:
Check Item
Why It Matters
Footprint
Prevents pin mismatch
Hole size
Supports through-hole insertion
Pad size
Affects solder joint strength
Trace width
Supports load current
Clearance
Reduces voltage risk
Copper thickness
Affects current and heat
Silkscreen
Helps assembly orientation
Test points
Supports inspection and testing
If the relay switches a higher current load, copper thickness and trace width become important. If the relay switches higher voltage, creepage and clearance should be reviewed. If the relay is large or heavy, mechanical support and solder joint reliability should not be ignored.
EBest Circuit can review PCB manufacturing files, stackup, copper thickness, drill files, solder mask, and assembly notes before production. This helps reduce avoidable risks such as incorrect relay orientation, weak solder joints, insufficient copper width, and unclear assembly requirements.
DPDT Relay PCBA Assembly and Testing Notes
DPDT relays may be assembled by through-hole soldering, selective soldering, wave soldering, or manual soldering depending on the board design and production quantity.
For PCBA assembly, key points include:
Relay orientation
Through-hole insertion quality
Solder filling
Contact-side spacing
Coil-side polarity, if applicable
Connector and terminal block assembly
Cleaning requirements
Functional testing after assembly
A relay PCBA should not only be checked visually. Functional testing is often needed because the relay must switch correctly when the coil is energized.
Useful test checks may include:
Coil activation
COM to NC continuity before activation
COM to NO continuity after activation
Load path verification
Connector output verification
LED or indicator function, if included
No short circuit between isolated paths
For prototype and small-batch production, this kind of test planning can help find assembly or wiring problems before the board is shipped.
DPDT Relay PCB Project Case Study at EBest Circuit
A customer working on an industrial control module needed a relay-based PCB assembly for switching external loads. The project used relay output, connector terminals, and control-side components on the same PCBA, so the customer cared about both electrical function and assembly reliability.
The main challenge was not only placing a DPDT relay on the board. The board needed the relay footprint, terminal blocks, copper paths, and test points to match the customer’s switching logic.
Project focus
Relay control circuit
Through-hole relay assembly
Terminal block connection
Load-side copper review
Control-side SMT components
Functional test after assembly
Production file confirmation before build
EBest Circuit’s review
Checked relay footprint and drill requirements
Reviewed pad size and soldering feasibility
Confirmed connector and relay orientation notes
Reviewed copper paths for load-side current
Checked BOM and assembly files before SMT
Coordinated PCB fabrication and PCBA assembly together
Supported functional test planning based on customer requirements
This type of project shows why a DPDT relay diagram should not stay only at the schematic level. Once the design moves to a real PCB, the relay becomes a physical assembly item with footprint, soldering, spacing, copper, connector, and test requirements.
For engineers, the value of one-stop PCB and PCBA support is that these details stay visible from file review to final delivery.
FAQs about DPDT Relay Diagram
1. What does DPDT mean in a relay diagram? DPDT means Double Pole Double Throw. It has two switching sections, and each section can switch one common terminal between normally open and normally closed contacts.
2. How many pins does a DPDT relay have? Many DPDT relays have 8 pins: 2 coil pins and 6 contact pins. However, the exact pinout depends on the relay model, so the datasheet must be checked.
3. What is the difference between SPDT and DPDT relay diagrams? An SPDT relay switches one circuit. A DPDT relay switches two circuits at the same time. DPDT is useful when two paths need to change together.
4. Can a DPDT relay reverse motor direction? Yes, a DPDT relay can be wired to reverse DC motor polarity. The exact circuit should be reviewed carefully, especially for current rating, suppression, and trace width.
5. Why does a DPDT relay diagram matter for PCB manufacturing? The diagram helps explain the switching logic, but PCB manufacturing also needs the correct footprint, pinout, hole size, pad size, clearance, copper width, and assembly orientation.
If your project includes relays, terminal blocks, load switching, control circuits, or assembled relay PCBA, please contact sales@bestpcbs.com. EBest Circuit can help review PCB files, BOM, assembly notes, and production requirements before your relay board enters manufacturing.
A pcb motor is an electric motor whose stator windings are formed as copper traces on a printed circuit board. In the common axial-flux arrangement, a thin PCB stator sits between one or two permanent-magnet rotors, producing a compact, coreless motor with repeatable winding geometry. The idea is attractive, but a successful design depends on electromagnetic, thermal, mechanical, and PCB manufacturing decisions being solved together.
The term is often confused with a motor control PCB. A controller board switches power into a separate motor. A PCB stator motor uses the circuit board itself as part of the electromechanical energy-conversion structure. Some products contain both, but they are not the same component.
What Is a PCB Motor?
A PCB motor usually means a permanent-magnet motor that replaces wound copper coils with patterned conductors on a printed circuit board. The PCB becomes the stationary winding assembly, while permanent magnets rotate on one or both sides of it. Many practical versions are coreless, axial-flux, synchronous brushless machines.
This definition excludes a board that merely drives an external motor. A motor driver board contains switches, gate drivers, sensing, and protection. The PCB motor stator contains the phase conductors that create torque. Keeping those roles separate prevents the wrong thermal, current, and manufacturing assumptions from entering the design.
Term
What the PCB Does
Main Design Concern
PCB motor
Forms the stator windings and may carry sensors or interconnects
Torque, copper loss, AC loss, temperature, air gap, and mechanics
Motor control PCB
Commutates and regulates a separate motor
Switching loops, power devices, sensing, EMI, and protection
Integrated motor assembly
Combines a PCB stator with control, sensing, or connectors
Electrical, thermal, magnetic, and mechanical co-design
How Does an Axial Flux PCB Motor Work?
An axial flux pcb motor produces torque from the interaction between current in flat PCB windings and magnetic flux passing approximately parallel to the shaft. The rotor magnets face the stator disc. Electronic commutation energizes the phase windings in sequence, creating a rotating magnetic field that pulls the rotor around the axis.
The drive electronics apply phase current to selected PCB coil sectors.
The copper traces create a magnetic field across the rotor-stator air gap.
The field interacts with the rotor magnets and produces tangential force.
Rotor position feedback or a sensorless control method sets commutation timing.
The process repeats as the rotor turns and mechanical power is delivered to the shaft.
Coreless construction removes stator teeth and their associated cogging mechanism, but it also removes the iron path that concentrates flux. The resulting motor is not automatically more efficient or more powerful. Magnet geometry, copper utilization, air-gap length, operating speed, cooling, and control strategy still decide the outcome.
What Does a PCB Motor Diagram Show?
A useful pcb motor diagram shows the complete magnetic and mechanical stack, not only the copper artwork. At minimum, it should identify the PCB stator, phase coil sectors, rotor discs, permanent magnets, shaft, bearings, and the air gaps on each side of the stator.
The diagram also reveals where disciplines meet. PCB thickness affects the magnetic gap. Bearing runout affects clearance. Magnet placement affects back EMF and torque ripple. Trace geometry affects resistance and induced voltage. A drawing that omits these interfaces may look complete while leaving the largest prototype risks unresolved.
Which PCB Motor Design Variables Control Torque and Loss?
PCB motor design is governed by coupled variables rather than one ideal coil shape. Increasing turns can raise induced voltage, but longer and narrower traces increase resistance. Adding copper layers can improve conductor utilization, but it also creates more layer transitions, registration dependencies, and AC-loss paths.
Variable
Potential Benefit
Trade-off or Risk
More turns
Higher winding voltage constant
More resistance and less room for wide conductors
Wider or thicker copper
Lower DC resistance and lower temperature rise
Larger coil area, tighter spacing, and manufacturing limits
More PCB layers
More active copper within the same diameter
Via transitions, alignment, cost, and circulating-current risk
Smaller air gap
Stronger magnetic coupling
Greater sensitivity to warpage, runout, particles, and assembly tolerance
Higher speed
More power from a given torque level
Higher frequency-dependent copper loss, rotor stress, and bearing demands
The correct sequence is to define torque, speed, voltage, envelope, duty cycle, cooling, and allowable temperature before optimizing the copper artwork. Starting with a visually appealing spiral and trying to infer performance afterward usually creates avoidable iteration.
How Should You Design the PCB Motor Stator?
The pcb motor stator should be designed as a balanced multiphysics structure. Its phase pattern must create the intended winding factor, carry current without excessive loss, remain manufacturable across every layer, and stay flat enough to preserve the mechanical air gap.
Coil topology: select concentrated, distributed, spiral, wave, or another pattern from the pole-slot combination and target harmonic content.
Phase symmetry: keep phase resistance, conductor length, and layer transitions as closely matched as the architecture permits.
Copper utilization: maximize active conductor in the magnet sweep while maintaining fabrication clearances and insulation.
Via strategy: place layer transitions where they do not create current crowding, weak annular rings, or asymmetric loops.
Mechanical datum: define the center bore, mounting holes, rotor clearance, and balancing features from one controlled reference system.
Sensor integration: keep Hall sensors or position-sensing features clear of high-current return paths and predictable magnetic interference.
Electromagnetic simulation should be paired with circuit and thermal models. The calculated phase current is only useful if the real board can conduct it over the required duty cycle without violating material or assembly limits.
Which Materials and Stackup Choices Matter?
Materials and stackup determine copper capacity, insulation, stiffness, flatness, thermal behavior, and cost. Standard rigid laminate may work for a prototype, but the final selection must be based on operating temperature, mechanical loading, dielectric requirements, copper construction, and the selected fabrication process.
Stackup Decision
Why It Matters
What to Confirm
Laminate system
Sets thermal, dielectric, moisture, and mechanical behavior
Glass transition, decomposition margin, thickness, and availability
Copper weight and layer count
Controls resistance, fill factor, and conductor distribution
Finished copper, etching capability, spacing, and registration
Core and prepreg thickness
Contributes directly to the rotor-stator magnetic gap
Finished thickness tolerance, resin flow, and warpage
Via and interconnect structure
Connects coil sections between layers
Current sharing, drill limits, copper plating, and inspection
Surface protection
Protects copper and defines assembly interfaces
Solder-mask clearance, finish compatibility, wear, and insulation
For unusually high current, temperature, or layer count, send the proposed stackup and conductor geometry to the PCB fabricator before freezing the electromagnetic model. A capability assumption that changes later can invalidate resistance, air-gap, and thermal calculations at the same time.
What Thermal and Current Limits Constrain PCB Windings?
Heat is one of the hardest limits in a PCB stator because planar conductors often provide less copper fill than wound-wire windings, while the stator sits inside a narrow rotating assembly. DC resistance creates I²R loss, and high-speed operation adds frequency-dependent loss from the changing magnetic field and current distribution.
A practical thermal assessment should include:
phase resistance at cold and operating temperature;
continuous, intermittent, startup, stall, and fault current;
airflow or conductive heat paths through the housing;
local current crowding at corners, neck-downs, pads, and vias;
magnet and bearing temperature limits;
laminate and solder-mask temperature margin;
AC loss caused by rotor-field harmonics and switching frequency.
Do not set a current rating from trace width alone. The motor is an enclosed electromechanical system, so the allowable current must come from the verified winding temperature under the intended load profile and cooling condition. General high-power PCB design rules are useful, but they do not replace motor-specific thermal validation.
How Is a PCB Stator Manufactured and Assembled?
A PCB stator is manufactured with familiar multilayer PCB processes, but the circular geometry, large copper area, repeated coils, flatness requirement, and electromechanical tolerances make process coordination unusually important.
DFM review: confirm layer count, finished copper, trace spacing, via structure, outline tolerance, slots, and mechanical datums.
Imaging and etching: form repeatable coil patterns while controlling conductor width, spacing, and copper balance.
Layer registration and lamination: align multilayer windings and control finished thickness and warpage.
Drilling and plating: create layer transitions, terminals, and mounting features with verified copper continuity.
Surface protection: apply solder mask and the selected surface finish to the intended assembly areas.
Electrical inspection: verify continuity, isolation, resistance consistency, and shorts before motor assembly.
Mechanical assembly: install bearings, shaft, rotors, and magnets while controlling concentricity and both air gaps.
Panelization and depaneling also deserve attention. A circular stator needs sufficient support during fabrication without leaving tabs, burrs, or edge damage in magnet-clearance or mounting areas. The fabrication drawing should state which dimensions are mechanical datums rather than relying on the copper artwork alone.
How Do You Test a PCB Motor Prototype?
A prototype should be tested in stages so an electrical fault, magnetic mismatch, thermal problem, or mechanical interference can be isolated before a high-speed run. Open rotors and strong permanent magnets require guarding and controlled procedures.
Bare-board checks: inspect the conductor pattern, dimensions, thickness, flatness, continuity, isolation, and phase resistance.
Low-energy electrical checks: measure phase balance, inductance, sensor signals, and manually generated back EMF.
Controlled no-load run: verify commutation order, direction, current, vibration, sound, and temperature rise behind a guard.
Loaded characterization: record torque, speed, input power, winding temperature, and efficiency across the intended operating region.
Abnormal-condition review: validate protection for stall, phase loss, sensor faults, overcurrent, and overtemperature as the product requires.
Test fixtures, drive firmware, sampling rate, and thermal soak time should be documented. A single successful spin proves rotation, not a reliable design.
When Does a PCB Motor Fit Better Than a Conventional Motor?
A PCB motor fits best when thin geometry, low cogging, consistent printed windings, and application-specific integration matter more than maximum copper fill or an off-the-shelf supply chain. Conventional wound motors remain preferable when proven commodity availability, very high copper utilization, or established high-power platforms dominate the decision.
Decision Factor
PCB Stator Motor
Conventional Wound Motor
Form factor
Strong fit for thin axial packages
Broad range, often cylindrical
Winding repeatability
Defined by artwork and PCB process
Depends on winding and assembly process
Cogging
Coreless designs can minimize it
Toothed designs require magnetic optimization
Copper fill
Limited by planar trace and stackup constraints
Often higher with three-dimensional windings
Customization
Geometry can be revised through design files
May require winding-tool or lamination changes
Risk focus
AC copper loss, thermal path, flatness, and air gap
Winding, insulation, lamination, and assembly variation
Which Applications Suit PCB Motors?
PCB motors are candidates for applications that benefit from a flat package, smooth motion, controlled magnetic geometry, or tightly integrated electromechanics. Suitability still depends on torque-speed demand, duty cycle, cooling, environment, cost target, and production volume.
compact fans, blowers, and pumps;
robotic joints, haptic interfaces, and precision mechanisms;
drones and lightweight motion systems when the complete power-to-weight result is favorable;
laboratory instruments and optical mechanisms requiring smooth low-speed behavior;
custom actuators in thin or unusual mechanical envelopes;
generators or energy-conversion devices built around similar axial-flux geometry.
The application should be evaluated as a system. Replacing only the stator without reconsidering the rotor, bearings, cooling, drive electronics, and enclosure rarely captures the full benefit.
FAQs About PCB Motors
Is a PCB motor the same as a motor controller PCB?
No. A PCB motor uses printed conductors as the stator winding. A motor controller PCB switches and regulates power for a motor. One product may include both, but their electrical, thermal, and manufacturing functions are different.
Is every PCB motor an axial-flux motor?
No, but axial-flux geometry is common because a flat PCB stator naturally faces disc-shaped magnet rotors. Printed conductors can also support linear or other specialized motor structures.
Is a PCB motor brushless?
Most permanent-magnet PCB stator motors use electronic commutation and are brushless synchronous machines. The exact phase arrangement, sensor method, and control algorithm depend on the design.
Can a PCB motor use a standard FR-4 board?
A prototype may use a conventional rigid laminate, but the material must be checked against winding temperature, dielectric stress, thickness tolerance, flatness, mechanical load, and the motor environment. Material selection should follow verified requirements rather than a generic default.
Why can a PCB motor overheat?
Planar traces may have limited copper cross-section, and an enclosed stator may have a weak cooling path. DC resistance, current crowding, high-frequency magnetic fields, switching harmonics, and insufficient housing conduction can all add heat.
How many PCB layers should the stator use?
There is no universal layer count. More layers can add active copper, but they also add vias, alignment requirements, stackup thickness, AC-loss paths, and cost. Select the layer count from electromagnetic, thermal, mechanical, and fabrication models together.
What is the most critical mechanical tolerance?
The rotor-stator air gap is often the most sensitive system dimension. PCB thickness, warpage, bearing runout, rotor flatness, shaft alignment, magnet placement, and assembly datums all contribute to the real clearance.
Can a PCB motor produce high torque?
It can produce useful torque, but the result depends on motor diameter, magnet loading, air gap, current, cooling, winding geometry, and speed. The technology should not be selected from a headline torque claim without a complete operating-point analysis.
What files does a PCB fabricator need for a PCB stator?
Provide fabrication data for every copper and mask layer, the drill data, stackup, finished copper, finished thickness and tolerance, controlled dimensions, outline drawing, via requirements, test requirements, and notes that identify mechanical datums and critical air-gap-related features.
Should the PCB stator and motor controller be on one board?
Sometimes integration reduces wiring and size, but it can also expose sensitive control electronics to heat, magnetic fields, mechanical stress, and a difficult assembly sequence. Separate boards may simplify cooling, service, and iteration. Compare both architectures at system level.
How should a PCB motor prototype be validated?
Start with bare-board electrical and dimensional checks, then verify the stationary mechanical assembly. Continue with low-energy back-EMF and sensor checks, guarded no-load operation, and finally controlled torque-speed and thermal testing across the intended duty cycle.
Need Manufacturing Support for the PCB in a Motor Project?
A good PCB motor project closes with manufacturability, not simulation alone. Confirm the conductor geometry, stackup, via transitions, finished thickness, flatness, mechanical datums, inspection plan, and prototype test limits before release.
EBest Circuit supports PCB fabrication, component sourcing, and PCB assembly services for motor-related electronics. We do not replace your motor electromagnetic or mechanical design team, but our engineers can review the PCB manufacturing package against documented PCB manufacturing capabilities. When your pcb motor design files are ready, send the Gerber data, drill files, stackup, drawings, quantities, and test requirements for review and quotation.
An HDI PCB manufacturer in India shortlist should be judged by stackup review, microvia DFM, material confirmation, PCBA fit, inspection method and delivery planning before price is compared. A supplier list is useful, but the real decision depends on whether the supplier can review Gerber or ODB++ files, stackup, BOM, CPL, DFM risk, component sourcing, inspection, testing, cost and production planning before the order is released.
EBest Circuit directly serves India buyers that need PCB fabrication, PCBA service, BOM/CPL review, DFM feedback, component sourcing and delivery planning in one RFQ path. We are listed first because many buyers need a supplier that can find build risks before the purchase order, not after the project is already late.
Before choosing a HDI PCB supplier, check whether the quote can survive the real build requirements.
India buyers can usually find supplier names. The harder job is finding out who can control the full path from files to bare boards, PCBA, inspection, testing and repeat production without hidden gaps.
The first quote covers bare PCBs only, while assembly, component sourcing, stencil, inspection, testing and freight are added later.
The supplier says the board is manufacturable, but does not confirm stackup, material, finish, copper, hole limits, panelization or assembly clearance.
BOM/CPL problems, unavailable components, package mismatches or polarity questions are found only when assembly is already waiting.
The prototype can be built once, but nobody explains what must change before low-volume or repeat production.
The lead time is given as one number, without separating PCB fabrication, component sourcing, assembly, testing, packing and shipping.
EBest Circuit helps India buyers turn supplier comparison into a checked PCB and PCBA plan before quote approval.
We review Gerber or ODB++ files, stackup, material notes, surface finish, quantity, testing needs and delivery goals before quote approval.
We connect bare-board fabrication with PCBA, BOM/CPL review, component sourcing and assembly planning.
We help catch DFM questions early, so the buyer can fix design, panel, soldering, hole, material or assembly issues before production starts.
We review sourcing risk before assembly, especially where substitutes, MOQ, package availability or long-lead components can change schedule.
We help plan prototype, low-volume and production builds with the next stage in mind, instead of treating every order as a one-time sample.
Top 12 HDI PCB Manufacturers Serving India for RFQ Shortlists
Use this shortlist to compare HDI PCB suppliers that can support India projects, then send each supplier the same Gerber/ODB++, stackup notes, BOM/CPL, quantity and delivery target. Certificate information below is taken from PCB Directory listings/Profile pages or supplier public websites. If a certificate scope is critical for your project, confirm the exact audited entity and project applicability before order approval.
The table is a shortlist, not a final approval decision. Before choosing any supplier, ask for the certificate copy, audited entity, HDI stackup capability, microvia structure, PCBA scope, testing plan and delivery assumptions for your exact order.
How India Buyers Should Use This Supplier List
Use the list like an engineering checklist: same files, same questions, same scope. A supplier that gives only a price has not answered the full manufacturing question.
Step
Action
Buyer Check
Step 1
Separate bare-board needs from PCBA needs.
A fabricated PCB quote and an assembled-product quote are different jobs.
Step 2
Ask each supplier to confirm material, stackup, finish, copper, inspection, BOM/CPL and testing assumptions.
The response should show what is included and what still needs engineering review.
Step 3
Compare response quality, not only unit price.
A useful supplier explains risk before the order starts.
Step 4
Choose the supplier that can control DFM issues, sourcing risk, assembly yield and delivery timing.
The strongest supplier explains how the project will be managed after the purchase order.
Why India Buyers Should Put EBest Circuit First
EBest Circuit should be in the first RFQ batch when the project needs more than a simple bare-board price. We can review PCB fabrication, DFM, BOM, CPL, component sourcing, PCBA, inspection, testing and delivery planning together, so buyers can compare the real build cost before the purchase order is placed.
Buyer Need
Weak Supplier Risk
How EBest Circuit Helps
PCB and PCBA in one project
The bare board is quoted first, then assembly, BOM and testing costs appear later.
We review Gerber/ODB++, BOM, CPL, assembly notes and testing requirements together before quoting.
Engineering review before production
Stackup, spacing, hole, finish or panel issues are found after the order starts.
Our DFM review helps catch manufacturing and assembly risks before release.
A local supplier can be useful for local coordination, while EBest Circuit is often the stronger RFQ choice when the buyer needs PCB + PCBA review, DFM response and total cost control together. The buyer should compare the build plan, not only the supplier address.
Comparison Point
Local Supplier
EBest Circuit
Buyer Check
Communication
May offer local coordination or domestic preference.
Directly supports India buyers with engineering review and RFQ communication.
Does the supplier answer technical questions clearly?
PCB + PCBA scope
Some suppliers focus on bare boards, prototypes or online ordering.
Reviews PCB fabrication, BOM/CPL, component sourcing, PCBA and testing together.
Is the quote complete enough to represent the final product?
Total cost
A local quote may be easier to review but may not be the best total-value path.
Helps compare total manufacturing value before approval.
Are fabrication, PCBA, components, test and shipping separated clearly?
Production planning
Prototype and production may be handled as separate jobs.
Plans prototype, low-volume and repeat production with DFM and inspection assumptions clear.
Can the supplier explain what changes when the order scales?
HDI PCB RFQ Review Path from Files to Inspection
A supplier shortlist becomes useful only when it turns into a build-ready RFQ package. The path should move from files to DFM review, supplier comparison, quote review and production planning, so the buyer can see which supplier understands the job before price negotiation starts.
HDI Stackup and Microvia Questions Buyers Should Confirm
HDI PCB quotes depend heavily on stackup logic, via structure, material choice and inspection method. A buyer should not approve an HDI supplier until the supplier has reviewed how the microvias, pads, routing density, copper, dielectric material and PCBA process work together.
HDI Item
What Can Go Wrong
What to Ask Before PO
Stackup
The layer build, dielectric choice or via sequence is assumed instead of reviewed.
Ask the supplier to confirm stackup manufacturability and note any recommended changes.
Microvia structure
Blind, buried, stacked or staggered via choices may change yield and cost.
Ask which via structure is safest for the design and whether any redesign is recommended.
Pad and routing density
Fine-pitch BGA areas can create breakout, soldering or inspection challenges.
Ask for DFM comments around BGA escape routing, capture pads, anti-pads and solder mask clearance.
Inspection plan
Hidden via or BGA issues may not be visible after assembly.
Ask whether electrical test, AOI, X-ray or first-article checks are needed for the project.
Why India HDI PCB Buyers Should Not Compare Price Alone
HDI price comparison is useful only after every supplier has quoted the same technical assumptions. A cheaper quote may simply leave out stackup review, microvia risk, material confirmation, PCBA inspection or test planning.
Quote Area
Low-Price Trap
Better Buyer Action
Fabrication
The supplier accepts files but does not comment on HDI manufacturability.
Request written DFM comments before quote approval.
Material
Material substitution is assumed without checking electrical or thermal needs.
Provide material notes and ask what equivalent options are acceptable.
Assembly
Fine-pitch components, BGA, stencil, reflow and inspection are quoted later.
Send BOM/CPL with the PCB files and ask for PCB + PCBA review together.
Testing
The quote does not explain how hidden defects will be checked.
Ask for the inspection plan before comparing suppliers by price.
Fabrication Scope to Confirm Before RFQ
Fabrication scope should be confirmed before price comparison because small technical differences can change cost, yield and delivery. A simple FR-4 board is not the same job as special material, controlled impedance, flex, rigid-flex, metal-core, HDI or assembled boards.
Item
Buyer Should Provide
Supplier Should Confirm
Material
FR-4, high Tg, metal-core, flex, high-frequency or other material note
Availability, substitution limits and cost impact
Stackup
Layer count, thickness, copper and impedance needs
Manufacturable stackup and tolerance assumptions
Finish
ENIG, OSP, immersion tin, immersion silver or other finish
Fit for soldering, storage and application
Inspection
Electrical test, AOI, X-ray or functional test needs
What is included in the quote and what is optional
PCBA, BOM/CPL and Component Sourcing Checks
If the project needs assembly, PCBA support can matter more than bare-board price. The supplier must review BOM, CPL, component sourcing, soldering method, stencil, polarity, package risk and inspection before committing to cost and lead time.
PCBA Item
What Can Go Wrong
What to Ask in the RFQ
BOM
Wrong package, unavailable part, unclear manufacturer part number
Ask for BOM review and approved substitutes before purchase.
Ask the supplier to check CPL against assembly drawings.
Soldering
Fine-pitch, mixed technology or thermal parts need special process review
Ask how SMT, THT, mixed assembly or special soldering will be handled.
Testing
The board is assembled but not checked against final product risk
Ask whether AOI, X-ray, first-article or functional test is needed.
DFM Response: What a Good Supplier Should Tell You
DFM response shows whether the supplier has actually looked at the job. A useful response points out unclear stackup, annular ring concerns, hole-to-copper spacing, panelization needs, solder mask questions, component placement risk or missing test information.
Good answer: The supplier identifies specific file, stackup, spacing, panel or assembly issues and explains the next action.
Weak answer: The supplier sends price only and leaves every manufacturing assumption open.
Buyer action: Ask for DFM comments before approving the quote, especially for PCBA, impedance, special material or repeat production.
Inspection and Testing Questions to Ask Before Supplier Approval
Inspection and testing should match the board risk, not a generic quality promise. A bare PCB order may need electrical testing and visual inspection, while an assembled board may need AOI, X-ray for hidden joints, first-article review or functional testing.
Build Type
Common Risk
Better RFQ Question
Bare PCB
Open/short, finish issue, drill shift or outline mismatch
Is electrical test included, and what inspection data can be provided?
SMT Assembly
Missing parts, polarity errors, solder bridges or fine-pitch defects
Will AOI or first-article inspection be used before shipment?
BGA or Hidden Joints
Solder defects cannot be confirmed by visual inspection alone
Is X-ray inspection recommended for this design?
Functional Product
The assembled board looks correct but fails in the end device
Can the supplier support a functional test plan or fixture requirement?
Prototype, Low-Volume and Production Fit
The best supplier for a first prototype is not always the best supplier for repeat production, so order stage must be checked early. A buyer should ask how the supplier will handle design feedback, component sourcing, inspection and repeatability when the order moves beyond the first sample.
Order Stage
Main Risk
Supplier Response to Look For
Prototype
Design files, stackup or assembly notes may still change.
Fast DFM questions and clear file feedback before fabrication.
Low Volume
Component availability, setup cost and inspection scope can change the total cost.
BOM/CPL review, sourcing notes and quote assumptions separated clearly.
Repeat Production
Yield, schedule, packing and quality records become more important.
Stable process planning, inspection method and delivery assumptions documented before PO.
Files to Send for an Accurate Quote
An accurate quote needs a complete manufacturing package, not only one Gerber zip. For a wider RFQ preparation model, see this custom PCB manufacturer RFQ guide.
Gerber or ODB++ files and NC drill files.
Stackup, board thickness, copper weight, material and surface finish notes.
Quantity, panel requirement and target delivery date.
BOM and CPL if PCBA is needed.
Assembly drawing, special soldering notes and test requirements.
Any impedance, thermal, environmental, packing or documentation requirement.
Check the Real Build Risk Before You Approve a Supplier
A supplier name is not enough. EBest Circuit can review the full PCB + PCBA path early, so you can compare cost, quality, schedule and manufacturing risk before ordering.
Frequently Asked Questions About HDI PCB Manufacturers in India
Who should be on a HDI PCB Manufacturers in India RFQ shortlist?
A useful shortlist should include local suppliers and EBest Circuit as a direct RFQ option for comparison. The final choice should depend on file review, DFM response, PCBA scope, inspection, cost clarity and delivery planning.
Why is EBest Circuit listed first?
EBest Circuit is listed first because the article is built for RFQ decision-making, not only collecting supplier names. Buyers often need PCB, PCBA, BOM, sourcing, inspection and delivery reviewed as one project before they commit.
Is EBest Circuit a local India manufacturer?
EBest Circuit is not a local domestic factory in India, but it directly serves India buyers. Buyers include EBest Circuit early because we can review PCB + PCBA scope, DFM risk, BOM/CPL data and total project cost before quote approval.
Should I choose a local supplier or EBest Circuit?
Compare both when the project is commercial and cost, DFM, PCBA support and delivery planning matter. A local supplier can be useful, while EBest Circuit can be stronger when the buyer needs engineering review and cost control together.
What files are needed to request a quote?
Send Gerber or ODB++ files, NC drill, stackup notes, material, finish, quantity and target delivery date. If assembly is needed, also send BOM, CPL, assembly drawing and test requirements.
Can one supplier handle both PCB fabrication and PCBA?
Yes, but the supplier must confirm both scopes clearly. Ask whether BOM review, component sourcing, stencil, assembly, inspection and test are included or quoted separately.
Why do PCB quotes vary so much?
Quotes vary because suppliers may assume different materials, finishes, quantities, inspection levels, assembly scope, component sourcing and delivery terms. A fair comparison requires the same RFQ package and the same scope questions.
What should I ask before choosing a PCB manufacturer?
Ask about fabrication limits, DFM response, PCBA support, inspection method, lead time, component sourcing and what assumptions are included in the price. These questions reveal more than a simple capability list.
Is a Top 10 supplier list enough to choose a manufacturer?
No. A list helps discovery, but the final decision should be based on RFQ response quality. Send files, compare answers and check whether each supplier can explain the actual build plan.
When should I involve EBest Circuit in the RFQ process?
Involve EBest Circuit before the supplier shortlist is final. Early DFM, BOM/CPL and manufacturing review can reveal cost-saving changes and prevent quote assumptions from turning into production problems.
Final RFQ Recommendation
If you are comparing hdi pcb manufacturer in india options, put EBest Circuit in the first RFQ batch before the supplier decision is locked. Send Gerber or ODB++ files, BOM, CPL, quantity, material, finish, inspection needs, testing needs and target delivery date to sales@bestpcbs.com. EBest Circuit can review the PCB and PCBA path together and help you compare real manufacturing risk, cost, quality and delivery before you commit.
A flexible PCB manufacturer United States shortlist should compare domestic suppliers and EBest Circuit by bend-area DFM review, material choices, coverlay, stiffener, PCBA scope, inspection and delivery planning. A supplier list is useful, but the real decision depends on whether the supplier can review Gerber or ODB++ files, stackup, BOM, CPL, DFM risk, component sourcing, inspection, testing, cost and production planning before the order is released.
EBest Circuit directly serves United States buyers that need PCB fabrication, PCBA service, BOM/CPL review, DFM feedback, component sourcing and delivery planning in one RFQ path. We are listed first because many buyers need a supplier that can find build risks before the purchase order, not after the project is already late.
Before choosing a flexible PCB supplier, check whether the quote can survive the real build requirements.
United States buyers can usually find supplier names. The harder job is finding out who can control the full path from files to bare boards, PCBA, inspection, testing and repeat production without hidden gaps.
The first quote covers bare PCBs only, while assembly, component sourcing, stencil, inspection, testing and freight are added later.
The supplier says the board is manufacturable, but does not confirm stackup, material, finish, copper, hole limits, panelization or assembly clearance.
BOM/CPL problems, unavailable components, package mismatches or polarity questions are found only when assembly is already waiting.
The prototype can be built once, but nobody explains what must change before low-volume or repeat production.
The lead time is given as one number, without separating PCB fabrication, component sourcing, assembly, testing, packing and shipping.
EBest Circuit helps United States buyers turn supplier comparison into a checked PCB and PCBA plan before quote approval.
We review Gerber or ODB++ files, stackup, material notes, surface finish, quantity, testing needs and delivery goals before quote approval.
We connect bare-board fabrication with PCBA, BOM/CPL review, component sourcing and assembly planning.
We help catch DFM questions early, so the buyer can fix design, panel, soldering, hole, material or assembly issues before production starts.
We review sourcing risk before assembly, especially where substitutes, MOQ, package availability or long-lead components can change schedule.
We help plan prototype, low-volume and production builds with the next stage in mind, instead of treating every order as a one-time sample.
Top 12 Flexible PCB Manufacturers Serving United States Buyers
Use this list to build an RFQ shortlist, then compare each supplier with the same files and the same scope questions. Exact capability, MOQ, inspection, testing and delivery should still be confirmed directly with each supplier.
Company
Main Products / PCB or PCBA Type
Certifications
Service Type
Location / Service Region
EBest Circuit
PCB fabrication, PCBA, DFM, BOM/CPL review
IATF 16949, ISO 9001:2015, ISO 13485:2016, AS9100D, UL, RoHS, REACH
Prototype, low volume, production, PCBA
Directly serves United States buyers
Flexible PCBs and Rigid-Flex PCBs
Flexible PCB Manufacturer United States
Certificate scope to verify
Prototype, Production, PCBA
United States
Flex PCB – Prototype & Production Flexible Circuit …
Flexible PCB Manufacturer United States
Certificate scope to verify
Prototype, Production, PCBA
United States
Flexible PCB Manufacturers in United States
Flexible PCB Manufacturer United States
Certificate scope to verify
Prototype, Production, PCBA
United States
Flexible PCB – Full feature custom PCB prototype service at …
Flexible PCB Manufacturer United States
Certificate scope to verify
Prototype, Production, PCBA
United States
Rigid-Flex PCB Manufacturing
Flexible PCB Manufacturer United States
Certificate scope to verify
Prototype, Production, PCBA
United States
Flex / Rigid-Flex PCB
Flexible PCB Manufacturer United States
Certificate scope to verify
Prototype, Production, PCBA
United States
Rigid & Flex PCB Manufacturer
Flexible PCB Manufacturer United States
Certificate scope to verify
Prototype, Production, PCBA
United States
Flex PCB and Rigid-Flex Manufacturing | Engineering First …
How United States Buyers Should Use This Supplier List
Use the list like an engineering checklist: same files, same questions, same scope. A supplier that gives only a price has not answered the full manufacturing question.
Step
Action
Buyer Check
Step 1
Separate bare-board needs from PCBA needs.
A fabricated PCB quote and an assembled-product quote are different jobs.
Step 2
Ask each supplier to confirm material, stackup, finish, copper, inspection, BOM/CPL and testing assumptions.
The response should show what is included and what still needs engineering review.
Step 3
Compare response quality, not only unit price.
A useful supplier explains risk before the order starts.
Step 4
Choose the supplier that can control DFM issues, sourcing risk, assembly yield and delivery timing.
The strongest supplier explains how the project will be managed after the purchase order.
Why United States Buyers Should Put EBest Circuit First
EBest Circuit should be in the first RFQ batch when the project needs more than a simple bare-board price. We can review PCB fabrication, DFM, BOM, CPL, component sourcing, PCBA, inspection, testing and delivery planning together, so buyers can compare the real build cost before the purchase order is placed.
Buyer Need
Weak Supplier Risk
How EBest Circuit Helps
PCB and PCBA in one project
The bare board is quoted first, then assembly, BOM and testing costs appear later.
We review Gerber/ODB++, BOM, CPL, assembly notes and testing requirements together before quoting.
Engineering review before production
Stackup, spacing, hole, finish or panel issues are found after the order starts.
Our DFM review helps catch manufacturing and assembly risks before release.
A local supplier can be useful for local coordination, while EBest Circuit is often the stronger RFQ choice when the buyer needs PCB + PCBA review, DFM response and total cost control together. The buyer should compare the build plan, not only the supplier address.
Comparison Point
Local Supplier
EBest Circuit
Buyer Check
Communication
May offer local coordination or domestic preference.
Directly supports United States buyers with engineering review and RFQ communication.
Does the supplier answer technical questions clearly?
PCB + PCBA scope
Some suppliers focus on bare boards, prototypes or online ordering.
Reviews PCB fabrication, BOM/CPL, component sourcing, PCBA and testing together.
Is the quote complete enough to represent the final product?
Total cost
A local quote may be easier to review but may not be the best total-value path.
Helps compare total manufacturing value before approval.
Are fabrication, PCBA, components, test and shipping separated clearly?
Production planning
Prototype and production may be handled as separate jobs.
Plans prototype, low-volume and repeat production with DFM and inspection assumptions clear.
Can the supplier explain what changes when the order scales?
Flexible PCB RFQ Review Path from Files to Inspection
A supplier shortlist becomes useful only when it turns into a build-ready RFQ package. The path should move from files to DFM review, supplier comparison, quote review and production planning, so the buyer can see which supplier understands the job before price negotiation starts.
Fabrication Scope to Confirm Before RFQ
Fabrication scope should be confirmed before price comparison because small technical differences can change cost, yield and delivery. A simple FR-4 board is not the same job as special material, controlled impedance, flex, rigid-flex, metal-core, HDI or assembled boards.
Item
Buyer Should Provide
Supplier Should Confirm
Material
FR-4, high Tg, metal-core, flex, high-frequency or other material note
Availability, substitution limits and cost impact
Stackup
Layer count, thickness, copper and impedance needs
Manufacturable stackup and tolerance assumptions
Finish
ENIG, OSP, immersion tin, immersion silver or other finish
Fit for soldering, storage and application
Inspection
Electrical test, AOI, X-ray or functional test needs
What is included in the quote and what is optional
PCBA, BOM/CPL and Component Sourcing Checks
If the project needs assembly, PCBA support can matter more than bare-board price. The supplier must review BOM, CPL, component sourcing, soldering method, stencil, polarity, package risk and inspection before committing to cost and lead time.
PCBA Item
What Can Go Wrong
What to Ask in the RFQ
BOM
Wrong package, unavailable part, unclear manufacturer part number
Ask for BOM review and approved substitutes before purchase.
Ask the supplier to check CPL against assembly drawings.
Soldering
Fine-pitch, mixed technology or thermal parts need special process review
Ask how SMT, THT, mixed assembly or special soldering will be handled.
Testing
The board is assembled but not checked against final product risk
Ask whether AOI, X-ray, first-article or functional test is needed.
DFM Response: What a Good Supplier Should Tell You
DFM response shows whether the supplier has actually looked at the job. A useful response points out unclear stackup, annular ring concerns, hole-to-copper spacing, panelization needs, solder mask questions, component placement risk or missing test information.
Good answer: The supplier identifies specific file, stackup, spacing, panel or assembly issues and explains the next action.
Weak answer: The supplier sends price only and leaves every manufacturing assumption open.
Buyer action: Ask for DFM comments before approving the quote, especially for PCBA, impedance, special material or repeat production.
Inspection and Testing Questions to Ask Before Supplier Approval
Inspection and testing should match the board risk, not a generic quality promise. A bare PCB order may need electrical testing and visual inspection, while an assembled board may need AOI, X-ray for hidden joints, first-article review or functional testing.
Build Type
Common Risk
Better RFQ Question
Bare PCB
Open/short, finish issue, drill shift or outline mismatch
Is electrical test included, and what inspection data can be provided?
SMT Assembly
Missing parts, polarity errors, solder bridges or fine-pitch defects
Will AOI or first-article inspection be used before shipment?
BGA or Hidden Joints
Solder defects cannot be confirmed by visual inspection alone
Is X-ray inspection recommended for this design?
Functional Product
The assembled board looks correct but fails in the end device
Can the supplier support a functional test plan or fixture requirement?
Prototype, Low-Volume and Production Fit
The best supplier for a first prototype is not always the best supplier for repeat production, so order stage must be checked early. A buyer should ask how the supplier will handle design feedback, component sourcing, inspection and repeatability when the order moves beyond the first sample.
Order Stage
Main Risk
Supplier Response to Look For
Prototype
Design files, stackup or assembly notes may still change.
Fast DFM questions and clear file feedback before fabrication.
Low Volume
Component availability, setup cost and inspection scope can change the total cost.
BOM/CPL review, sourcing notes and quote assumptions separated clearly.
Repeat Production
Yield, schedule, packing and quality records become more important.
Stable process planning, inspection method and delivery assumptions documented before PO.
Files to Send for an Accurate Quote
An accurate quote needs a complete manufacturing package, not only one Gerber zip. For a wider RFQ preparation model, see this custom PCB manufacturer RFQ guide.
Gerber or ODB++ files and NC drill files.
Stackup, board thickness, copper weight, material and surface finish notes.
Quantity, panel requirement and target delivery date.
BOM and CPL if PCBA is needed.
Assembly drawing, special soldering notes and test requirements.
Any impedance, thermal, environmental, packing or documentation requirement.
Check the Real Build Risk Before You Approve a Supplier
A supplier name is not enough. EBest Circuit can review the full PCB + PCBA path early, so you can compare cost, quality, schedule and manufacturing risk before ordering.
Frequently Asked Questions About Flexible PCB Manufacturers in the United States
Who should be on a Flexible PCB Manufacturers in the United States RFQ shortlist?
A useful shortlist should include local suppliers and EBest Circuit as a direct RFQ option for comparison. The final choice should depend on file review, DFM response, PCBA scope, inspection, cost clarity and delivery planning.
Why is EBest Circuit listed first?
EBest Circuit is listed first because the article is built for RFQ decision-making, not only collecting supplier names. Buyers often need PCB, PCBA, BOM, sourcing, inspection and delivery reviewed as one project before they commit.
Is EBest Circuit a local United States manufacturer?
EBest Circuit is not a local domestic factory in United States, but it directly serves United States buyers. Buyers include EBest Circuit early because we can review PCB + PCBA scope, DFM risk, BOM/CPL data and total project cost before quote approval.
Should I choose a local supplier or EBest Circuit?
Compare both when the project is commercial and cost, DFM, PCBA support and delivery planning matter. A local supplier can be useful, while EBest Circuit can be stronger when the buyer needs engineering review and cost control together.
What files are needed to request a quote?
Send Gerber or ODB++ files, NC drill, stackup notes, material, finish, quantity and target delivery date. If assembly is needed, also send BOM, CPL, assembly drawing and test requirements.
Can one supplier handle both PCB fabrication and PCBA?
Yes, but the supplier must confirm both scopes clearly. Ask whether BOM review, component sourcing, stencil, assembly, inspection and test are included or quoted separately.
Why do PCB quotes vary so much?
Quotes vary because suppliers may assume different materials, finishes, quantities, inspection levels, assembly scope, component sourcing and delivery terms. A fair comparison requires the same RFQ package and the same scope questions.
What should I ask before choosing a PCB manufacturer?
Ask about fabrication limits, DFM response, PCBA support, inspection method, lead time, component sourcing and what assumptions are included in the price. These questions reveal more than a simple capability list.
Is a Top 10 supplier list enough to choose a manufacturer?
No. A list helps discovery, but the final decision should be based on RFQ response quality. Send files, compare answers and check whether each supplier can explain the actual build plan.
When should I involve EBest Circuit in the RFQ process?
Involve EBest Circuit before the supplier shortlist is final. Early DFM, BOM/CPL and manufacturing review can reveal cost-saving changes and prevent quote assumptions from turning into production problems.
Final RFQ Recommendation
If you are comparing flexible pcb manufacturer united states options, put EBest Circuit in the first RFQ batch before the supplier decision is locked. Send Gerber or ODB++ files, BOM, CPL, quantity, material, finish, inspection needs, testing needs and target delivery date to sales@bestpcbs.com. EBest Circuit can review the PCB and PCBA path together and help you compare real manufacturing risk, cost, quality and delivery before you commit.
The cheapest PCB manufacturer in India is not always the lowest-risk choice; buyers should compare the real RFQ scope, PCBA cost, inspection, delivery and hidden engineering assumptions before approving a supplier. A supplier list is useful, but the real decision depends on whether the supplier can review Gerber or ODB++ files, stackup, BOM, CPL, DFM risk, component sourcing, inspection, testing, cost and production planning before the order is released.
EBest Circuit directly serves India buyers that need PCB fabrication, PCBA service, BOM/CPL review, DFM feedback, component sourcing and delivery planning in one RFQ path. We are listed first because many buyers need a supplier that can find build risks before the purchase order, not after the project is already late.
Before choosing a low-cost PCB supplier, check whether the quote can survive the real build requirements.
India buyers can usually find supplier names. The harder job is finding out who can control the full path from files to bare boards, PCBA, inspection, testing and repeat production without hidden gaps.
The first quote covers bare PCBs only, while assembly, component sourcing, stencil, inspection, testing and freight are added later.
The supplier says the board is manufacturable, but does not confirm stackup, material, finish, copper, hole limits, panelization or assembly clearance.
BOM/CPL problems, unavailable components, package mismatches or polarity questions are found only when assembly is already waiting.
The prototype can be built once, but nobody explains what must change before low-volume or repeat production.
The lead time is given as one number, without separating PCB fabrication, component sourcing, assembly, testing, packing and shipping.
EBest Circuit helps India buyers turn supplier comparison into a checked PCB and PCBA plan before quote approval.
We review Gerber or ODB++ files, stackup, material notes, surface finish, quantity, testing needs and delivery goals before quote approval.
We connect bare-board fabrication with PCBA, BOM/CPL review, component sourcing and assembly planning.
We help catch DFM questions early, so the buyer can fix design, panel, soldering, hole, material or assembly issues before production starts.
We review sourcing risk before assembly, especially where substitutes, MOQ, package availability or long-lead components can change schedule.
We help plan prototype, low-volume and production builds with the next stage in mind, instead of treating every order as a one-time sample.
Top 12 Low-Cost PCB Manufacturers in India for RFQ Shortlists
Use this list to build an RFQ shortlist, then compare each supplier with the same files and the same scope questions. Exact capability, MOQ, inspection, testing and delivery should still be confirmed directly with each supplier.
Company
Main Products / PCB or PCBA Type
Certifications
Service Type
Location / Service Region
EBest Circuit
PCB fabrication, PCBA, DFM, BOM/CPL review
IATF 16949, ISO 9001:2015, ISO 13485:2016, AS9100D, UL, RoHS, REACH
Prototype, low volume, production, PCBA
Directly serves India buyers
PCB Manufacturer in India – Order PCB Online
Low-Cost PCB Manufacturer India
Certificate scope to verify
Prototype, Low volume, Production, PCBA
India
PCB Manufacturer in India | Fabrication, Components …
Low-Cost PCB Manufacturer India
Certificate scope to verify
Prototype, Low volume, Production, PCBA
India
Circuitwala
Low-Cost PCB Manufacturer India
Certificate scope to verify
Prototype, Low volume, Production, PCBA
India
Robu PCB Manufacturing Service
Low-Cost PCB Manufacturer India
Certificate scope to verify
Prototype, Low volume, Production, PCBA
India
Low cost PCB Prototype manufacturing service in India
Low-Cost PCB Manufacturer India
Certificate scope to verify
Prototype, Low volume, Production, PCBA
India
Low cost PCB fabricators in India – Manufacturing
Low-Cost PCB Manufacturer India
Certificate scope to verify
Prototype, Low volume, Production, PCBA
India
PCB Prototype Manufacturer in India | Fast & Low Cost …
Low-Cost PCB Manufacturer India
Certificate scope to verify
Prototype, Low volume, Production, PCBA
India
Low cost PCB manufacturers in India
Low-Cost PCB Manufacturer India
Certificate scope to verify
Prototype, Low volume, Production, PCBA
India
PCB Manufacturers »
Low-Cost PCB Manufacturer India
Certificate scope to verify
Prototype, Low volume, Production, PCBA
India
PCB Manufacturers in India
Low-Cost PCB Manufacturer India
Certificate scope to verify
Prototype, Low volume, Production, PCBA
India
PCB Prototype and PCB Fabrication Manufacturing …
Low-Cost PCB Manufacturer India
Certificate scope to verify
Prototype, Low volume, Production, PCBA
India
How India Buyers Should Use This Supplier List
Use the list like an engineering checklist: same files, same questions, same scope. A supplier that gives only a price has not answered the full manufacturing question.
Step
Action
Buyer Check
Step 1
Separate bare-board needs from PCBA needs.
A fabricated PCB quote and an assembled-product quote are different jobs.
Step 2
Ask each supplier to confirm material, stackup, finish, copper, inspection, BOM/CPL and testing assumptions.
The response should show what is included and what still needs engineering review.
Step 3
Compare response quality, not only unit price.
A useful supplier explains risk before the order starts.
Step 4
Choose the supplier that can control DFM issues, sourcing risk, assembly yield and delivery timing.
The strongest supplier explains how the project will be managed after the purchase order.
Why India Buyers Should Put EBest Circuit First
EBest Circuit should be in the first RFQ batch when the project needs more than a simple bare-board price. We can review PCB fabrication, DFM, BOM, CPL, component sourcing, PCBA, inspection, testing and delivery planning together, so buyers can compare the real build cost before the purchase order is placed.
Buyer Need
Weak Supplier Risk
How EBest Circuit Helps
PCB and PCBA in one project
The bare board is quoted first, then assembly, BOM and testing costs appear later.
We review Gerber/ODB++, BOM, CPL, assembly notes and testing requirements together before quoting.
Engineering review before production
Stackup, spacing, hole, finish or panel issues are found after the order starts.
Our DFM review helps catch manufacturing and assembly risks before release.
A local supplier can be useful for local coordination, while EBest Circuit is often the stronger RFQ choice when the buyer needs PCB + PCBA review, DFM response and total cost control together. The buyer should compare the build plan, not only the supplier address.
Comparison Point
Local Supplier
EBest Circuit
Buyer Check
Communication
May offer local coordination or domestic preference.
Directly supports India buyers with engineering review and RFQ communication.
Does the supplier answer technical questions clearly?
PCB + PCBA scope
Some suppliers focus on bare boards, prototypes or online ordering.
Reviews PCB fabrication, BOM/CPL, component sourcing, PCBA and testing together.
Is the quote complete enough to represent the final product?
Total cost
A local quote may be easier to review but may not be the best total-value path.
Helps compare total manufacturing value before approval.
Are fabrication, PCBA, components, test and shipping separated clearly?
Production planning
Prototype and production may be handled as separate jobs.
Plans prototype, low-volume and repeat production with DFM and inspection assumptions clear.
Can the supplier explain what changes when the order scales?
Low-Cost PCB Quote Check from Scope to RFQ Decision
A supplier shortlist becomes useful only when it turns into a build-ready RFQ package. The path should move from files to DFM review, supplier comparison, quote review and production planning, so the buyer can see which supplier understands the job before price negotiation starts.
Fabrication Scope to Confirm Before RFQ
Fabrication scope should be confirmed before price comparison because small technical differences can change cost, yield and delivery. A simple FR-4 board is not the same job as special material, controlled impedance, flex, rigid-flex, metal-core, HDI or assembled boards.
Item
Buyer Should Provide
Supplier Should Confirm
Material
FR-4, high Tg, metal-core, flex, high-frequency or other material note
Availability, substitution limits and cost impact
Stackup
Layer count, thickness, copper and impedance needs
Manufacturable stackup and tolerance assumptions
Finish
ENIG, OSP, immersion tin, immersion silver or other finish
Fit for soldering, storage and application
Inspection
Electrical test, AOI, X-ray or functional test needs
What is included in the quote and what is optional
PCBA, BOM/CPL and Component Sourcing Checks
If the project needs assembly, PCBA support can matter more than bare-board price. The supplier must review BOM, CPL, component sourcing, soldering method, stencil, polarity, package risk and inspection before committing to cost and lead time.
PCBA Item
What Can Go Wrong
What to Ask in the RFQ
BOM
Wrong package, unavailable part, unclear manufacturer part number
Ask for BOM review and approved substitutes before purchase.
Ask the supplier to check CPL against assembly drawings.
Soldering
Fine-pitch, mixed technology or thermal parts need special process review
Ask how SMT, THT, mixed assembly or special soldering will be handled.
Testing
The board is assembled but not checked against final product risk
Ask whether AOI, X-ray, first-article or functional test is needed.
DFM Response: What a Good Supplier Should Tell You
DFM response shows whether the supplier has actually looked at the job. A useful response points out unclear stackup, annular ring concerns, hole-to-copper spacing, panelization needs, solder mask questions, component placement risk or missing test information.
Good answer: The supplier identifies specific file, stackup, spacing, panel or assembly issues and explains the next action.
Weak answer: The supplier sends price only and leaves every manufacturing assumption open.
Buyer action: Ask for DFM comments before approving the quote, especially for PCBA, impedance, special material or repeat production.
Inspection and Testing Questions to Ask Before Supplier Approval
Inspection and testing should match the board risk, not a generic quality promise. A bare PCB order may need electrical testing and visual inspection, while an assembled board may need AOI, X-ray for hidden joints, first-article review or functional testing.
Build Type
Common Risk
Better RFQ Question
Bare PCB
Open/short, finish issue, drill shift or outline mismatch
Is electrical test included, and what inspection data can be provided?
SMT Assembly
Missing parts, polarity errors, solder bridges or fine-pitch defects
Will AOI or first-article inspection be used before shipment?
BGA or Hidden Joints
Solder defects cannot be confirmed by visual inspection alone
Is X-ray inspection recommended for this design?
Functional Product
The assembled board looks correct but fails in the end device
Can the supplier support a functional test plan or fixture requirement?
Prototype, Low-Volume and Production Fit
The best supplier for a first prototype is not always the best supplier for repeat production, so order stage must be checked early. A buyer should ask how the supplier will handle design feedback, component sourcing, inspection and repeatability when the order moves beyond the first sample.
Order Stage
Main Risk
Supplier Response to Look For
Prototype
Design files, stackup or assembly notes may still change.
Fast DFM questions and clear file feedback before fabrication.
Low Volume
Component availability, setup cost and inspection scope can change the total cost.
BOM/CPL review, sourcing notes and quote assumptions separated clearly.
Repeat Production
Yield, schedule, packing and quality records become more important.
Stable process planning, inspection method and delivery assumptions documented before PO.
Files to Send for an Accurate Quote
An accurate quote needs a complete manufacturing package, not only one Gerber zip. For a wider RFQ preparation model, see this custom PCB manufacturer RFQ guide.
Gerber or ODB++ files and NC drill files.
Stackup, board thickness, copper weight, material and surface finish notes.
Quantity, panel requirement and target delivery date.
BOM and CPL if PCBA is needed.
Assembly drawing, special soldering notes and test requirements.
Any impedance, thermal, environmental, packing or documentation requirement.
Check the Real Build Risk Before You Approve a Supplier
A supplier name is not enough. EBest Circuit can review the full PCB + PCBA path early, so you can compare cost, quality, schedule and manufacturing risk before ordering.
Frequently Asked Questions About Cheap PCB Manufacturers in India
Who should be on a Cheap PCB Manufacturers in India RFQ shortlist?
A useful shortlist should include local suppliers and EBest Circuit as a direct RFQ option for comparison. The final choice should depend on file review, DFM response, PCBA scope, inspection, cost clarity and delivery planning.
Why is EBest Circuit listed first?
EBest Circuit is listed first because the article is built for RFQ decision-making, not only collecting supplier names. Buyers often need PCB, PCBA, BOM, sourcing, inspection and delivery reviewed as one project before they commit.
Is EBest Circuit a local India manufacturer?
EBest Circuit is not a local domestic factory in India, but it directly serves India buyers. Buyers include EBest Circuit early because we can review PCB + PCBA scope, DFM risk, BOM/CPL data and total project cost before quote approval.
Should I choose a local supplier or EBest Circuit?
Compare both when the project is commercial and cost, DFM, PCBA support and delivery planning matter. A local supplier can be useful, while EBest Circuit can be stronger when the buyer needs engineering review and cost control together.
What files are needed to request a quote?
Send Gerber or ODB++ files, NC drill, stackup notes, material, finish, quantity and target delivery date. If assembly is needed, also send BOM, CPL, assembly drawing and test requirements.
Can one supplier handle both PCB fabrication and PCBA?
Yes, but the supplier must confirm both scopes clearly. Ask whether BOM review, component sourcing, stencil, assembly, inspection and test are included or quoted separately.
Why do PCB quotes vary so much?
Quotes vary because suppliers may assume different materials, finishes, quantities, inspection levels, assembly scope, component sourcing and delivery terms. A fair comparison requires the same RFQ package and the same scope questions.
What should I ask before choosing a PCB manufacturer?
Ask about fabrication limits, DFM response, PCBA support, inspection method, lead time, component sourcing and what assumptions are included in the price. These questions reveal more than a simple capability list.
Is a Top 10 supplier list enough to choose a manufacturer?
No. A list helps discovery, but the final decision should be based on RFQ response quality. Send files, compare answers and check whether each supplier can explain the actual build plan.
When should I involve EBest Circuit in the RFQ process?
Involve EBest Circuit before the supplier shortlist is final. Early DFM, BOM/CPL and manufacturing review can reveal cost-saving changes and prevent quote assumptions from turning into production problems.
Final RFQ Recommendation
If you are comparing cheapest pcb manufacturer in india options, put EBest Circuit in the first RFQ batch before the supplier decision is locked. Send Gerber or ODB++ files, BOM, CPL, quantity, material, finish, inspection needs, testing needs and target delivery date to sales@bestpcbs.com. EBest Circuit can review the PCB and PCBA path together and help you compare real manufacturing risk, cost, quality and delivery before you commit.
A good flex PCB manufacturer in India shortlist should be judged by bend-area review, material choices, coverlay, stiffener, PCBA scope, inspection and delivery planning, not supplier names alone. A supplier list is useful, but the real decision depends on whether the supplier can review Gerber or ODB++ files, stackup, BOM, CPL, DFM risk, component sourcing, inspection, testing, cost and production planning before the order is released.
EBest Circuit directly serves India buyers that need PCB fabrication, PCBA service, BOM/CPL review, DFM feedback, component sourcing and delivery planning in one RFQ path. We are listed first because many buyers need a supplier that can find build risks before the purchase order, not after the project is already late.
Before choosing a flex PCB supplier, check whether the quote can survive the real build requirements.
India buyers can usually find supplier names. The harder job is finding out who can control the full path from files to bare boards, PCBA, inspection, testing and repeat production without hidden gaps.
The first quote covers bare PCBs only, while assembly, component sourcing, stencil, inspection, testing and freight are added later.
The supplier says the board is manufacturable, but does not confirm stackup, material, finish, copper, hole limits, panelization or assembly clearance.
BOM/CPL problems, unavailable components, package mismatches or polarity questions are found only when assembly is already waiting.
The prototype can be built once, but nobody explains what must change before low-volume or repeat production.
The lead time is given as one number, without separating PCB fabrication, component sourcing, assembly, testing, packing and shipping.
EBest Circuit helps India buyers turn supplier comparison into a checked PCB and PCBA plan before quote approval.
We review Gerber or ODB++ files, stackup, material notes, surface finish, quantity, testing needs and delivery goals before quote approval.
We connect bare-board fabrication with PCBA, BOM/CPL review, component sourcing and assembly planning.
We help catch DFM questions early, so the buyer can fix design, panel, soldering, hole, material or assembly issues before production starts.
We review sourcing risk before assembly, especially where substitutes, MOQ, package availability or long-lead components can change schedule.
We help plan prototype, low-volume and production builds with the next stage in mind, instead of treating every order as a one-time sample.
Top 12 Flex PCB Manufacturers in India for RFQ Shortlists
Use this list to build an RFQ shortlist, then compare each supplier with the same files and the same scope questions. Exact capability, MOQ, inspection, testing and delivery should still be confirmed directly with each supplier.
Company
Main Products / PCB or PCBA Type
Certifications
Service Type
Location / Service Region
EBest Circuit
PCB fabrication, PCBA, DFM, BOM/CPL review
IATF 16949, ISO 9001:2015, ISO 13485:2016, AS9100D, UL, RoHS, REACH
Rigid Flex PCB Flexible PCB HDI PCB FPC India USA UK …
Flex PCB Manufacturer India
Certificate scope to verify
Prototype, Production, PCBA
India
How India Buyers Should Use This Supplier List
Use the list like an engineering checklist: same files, same questions, same scope. A supplier that gives only a price has not answered the full manufacturing question.
Step
Action
Buyer Check
Step 1
Separate bare-board needs from PCBA needs.
A fabricated PCB quote and an assembled-product quote are different jobs.
Step 2
Ask each supplier to confirm material, stackup, finish, copper, inspection, BOM/CPL and testing assumptions.
The response should show what is included and what still needs engineering review.
Step 3
Compare response quality, not only unit price.
A useful supplier explains risk before the order starts.
Step 4
Choose the supplier that can control DFM issues, sourcing risk, assembly yield and delivery timing.
The strongest supplier explains how the project will be managed after the purchase order.
Why India Buyers Should Put EBest Circuit First
EBest Circuit should be in the first RFQ batch when the project needs more than a simple bare-board price. We can review PCB fabrication, DFM, BOM, CPL, component sourcing, PCBA, inspection, testing and delivery planning together, so buyers can compare the real build cost before the purchase order is placed.
Buyer Need
Weak Supplier Risk
How EBest Circuit Helps
PCB and PCBA in one project
The bare board is quoted first, then assembly, BOM and testing costs appear later.
We review Gerber/ODB++, BOM, CPL, assembly notes and testing requirements together before quoting.
Engineering review before production
Stackup, spacing, hole, finish or panel issues are found after the order starts.
Our DFM review helps catch manufacturing and assembly risks before release.
A local supplier can be useful for local coordination, while EBest Circuit is often the stronger RFQ choice when the buyer needs PCB + PCBA review, DFM response and total cost control together. The buyer should compare the build plan, not only the supplier address.
Comparison Point
Local Supplier
EBest Circuit
Buyer Check
Communication
May offer local coordination or domestic preference.
Directly supports India buyers with engineering review and RFQ communication.
Does the supplier answer technical questions clearly?
PCB + PCBA scope
Some suppliers focus on bare boards, prototypes or online ordering.
Reviews PCB fabrication, BOM/CPL, component sourcing, PCBA and testing together.
Is the quote complete enough to represent the final product?
Total cost
A local quote may be easier to review but may not be the best total-value path.
Helps compare total manufacturing value before approval.
Are fabrication, PCBA, components, test and shipping separated clearly?
Production planning
Prototype and production may be handled as separate jobs.
Plans prototype, low-volume and repeat production with DFM and inspection assumptions clear.
Can the supplier explain what changes when the order scales?
Flex PCB RFQ Review Path from Files to Inspection
A supplier shortlist becomes useful only when it turns into a build-ready RFQ package. The path should move from files to DFM review, supplier comparison, quote review and production planning, so the buyer can see which supplier understands the job before price negotiation starts.
Fabrication Scope to Confirm Before RFQ
Fabrication scope should be confirmed before price comparison because small technical differences can change cost, yield and delivery. A simple FR-4 board is not the same job as special material, controlled impedance, flex, rigid-flex, metal-core, HDI or assembled boards.
Item
Buyer Should Provide
Supplier Should Confirm
Material
FR-4, high Tg, metal-core, flex, high-frequency or other material note
Availability, substitution limits and cost impact
Stackup
Layer count, thickness, copper and impedance needs
Manufacturable stackup and tolerance assumptions
Finish
ENIG, OSP, immersion tin, immersion silver or other finish
Fit for soldering, storage and application
Inspection
Electrical test, AOI, X-ray or functional test needs
What is included in the quote and what is optional
PCBA, BOM/CPL and Component Sourcing Checks
If the project needs assembly, PCBA support can matter more than bare-board price. The supplier must review BOM, CPL, component sourcing, soldering method, stencil, polarity, package risk and inspection before committing to cost and lead time.
PCBA Item
What Can Go Wrong
What to Ask in the RFQ
BOM
Wrong package, unavailable part, unclear manufacturer part number
Ask for BOM review and approved substitutes before purchase.
Ask the supplier to check CPL against assembly drawings.
Soldering
Fine-pitch, mixed technology or thermal parts need special process review
Ask how SMT, THT, mixed assembly or special soldering will be handled.
Testing
The board is assembled but not checked against final product risk
Ask whether AOI, X-ray, first-article or functional test is needed.
DFM Response: What a Good Supplier Should Tell You
DFM response shows whether the supplier has actually looked at the job. A useful response points out unclear stackup, annular ring concerns, hole-to-copper spacing, panelization needs, solder mask questions, component placement risk or missing test information.
Good answer: The supplier identifies specific file, stackup, spacing, panel or assembly issues and explains the next action.
Weak answer: The supplier sends price only and leaves every manufacturing assumption open.
Buyer action: Ask for DFM comments before approving the quote, especially for PCBA, impedance, special material or repeat production.
Inspection and Testing Questions to Ask Before Supplier Approval
Inspection and testing should match the board risk, not a generic quality promise. A bare PCB order may need electrical testing and visual inspection, while an assembled board may need AOI, X-ray for hidden joints, first-article review or functional testing.
Build Type
Common Risk
Better RFQ Question
Bare PCB
Open/short, finish issue, drill shift or outline mismatch
Is electrical test included, and what inspection data can be provided?
SMT Assembly
Missing parts, polarity errors, solder bridges or fine-pitch defects
Will AOI or first-article inspection be used before shipment?
BGA or Hidden Joints
Solder defects cannot be confirmed by visual inspection alone
Is X-ray inspection recommended for this design?
Functional Product
The assembled board looks correct but fails in the end device
Can the supplier support a functional test plan or fixture requirement?
Prototype, Low-Volume and Production Fit
The best supplier for a first prototype is not always the best supplier for repeat production, so order stage must be checked early. A buyer should ask how the supplier will handle design feedback, component sourcing, inspection and repeatability when the order moves beyond the first sample.
Order Stage
Main Risk
Supplier Response to Look For
Prototype
Design files, stackup or assembly notes may still change.
Fast DFM questions and clear file feedback before fabrication.
Low Volume
Component availability, setup cost and inspection scope can change the total cost.
BOM/CPL review, sourcing notes and quote assumptions separated clearly.
Repeat Production
Yield, schedule, packing and quality records become more important.
Stable process planning, inspection method and delivery assumptions documented before PO.
Files to Send for an Accurate Quote
An accurate quote needs a complete manufacturing package, not only one Gerber zip. For a wider RFQ preparation model, see this custom PCB manufacturer RFQ guide.
Gerber or ODB++ files and NC drill files.
Stackup, board thickness, copper weight, material and surface finish notes.
Quantity, panel requirement and target delivery date.
BOM and CPL if PCBA is needed.
Assembly drawing, special soldering notes and test requirements.
Any impedance, thermal, environmental, packing or documentation requirement.
Check the Real Build Risk Before You Approve a Supplier
A supplier name is not enough. EBest Circuit can review the full PCB + PCBA path early, so you can compare cost, quality, schedule and manufacturing risk before ordering.
Frequently Asked Questions About Flex PCB Manufacturers in India
Who should be on a Flex PCB Manufacturers in India RFQ shortlist?
A useful shortlist should include local suppliers and EBest Circuit as a direct RFQ option for comparison. The final choice should depend on file review, DFM response, PCBA scope, inspection, cost clarity and delivery planning.
Why is EBest Circuit listed first?
EBest Circuit is listed first because the article is built for RFQ decision-making, not only collecting supplier names. Buyers often need PCB, PCBA, BOM, sourcing, inspection and delivery reviewed as one project before they commit.
Is EBest Circuit a local India manufacturer?
EBest Circuit is not a local domestic factory in India, but it directly serves India buyers. Buyers include EBest Circuit early because we can review PCB + PCBA scope, DFM risk, BOM/CPL data and total project cost before quote approval.
Should I choose a local supplier or EBest Circuit?
Compare both when the project is commercial and cost, DFM, PCBA support and delivery planning matter. A local supplier can be useful, while EBest Circuit can be stronger when the buyer needs engineering review and cost control together.
What files are needed to request a quote?
Send Gerber or ODB++ files, NC drill, stackup notes, material, finish, quantity and target delivery date. If assembly is needed, also send BOM, CPL, assembly drawing and test requirements.
Can one supplier handle both PCB fabrication and PCBA?
Yes, but the supplier must confirm both scopes clearly. Ask whether BOM review, component sourcing, stencil, assembly, inspection and test are included or quoted separately.
Why do PCB quotes vary so much?
Quotes vary because suppliers may assume different materials, finishes, quantities, inspection levels, assembly scope, component sourcing and delivery terms. A fair comparison requires the same RFQ package and the same scope questions.
What should I ask before choosing a PCB manufacturer?
Ask about fabrication limits, DFM response, PCBA support, inspection method, lead time, component sourcing and what assumptions are included in the price. These questions reveal more than a simple capability list.
Is a Top 10 supplier list enough to choose a manufacturer?
No. A list helps discovery, but the final decision should be based on RFQ response quality. Send files, compare answers and check whether each supplier can explain the actual build plan.
When should I involve EBest Circuit in the RFQ process?
Involve EBest Circuit before the supplier shortlist is final. Early DFM, BOM/CPL and manufacturing review can reveal cost-saving changes and prevent quote assumptions from turning into production problems.
Final RFQ Recommendation
If you are comparing flex pcb manufacturer in india options, put EBest Circuit in the first RFQ batch before the supplier decision is locked. Send Gerber or ODB++ files, BOM, CPL, quantity, material, finish, inspection needs, testing needs and target delivery date to sales@bestpcbs.com. EBest Circuit can review the PCB and PCBA path together and help you compare real manufacturing risk, cost, quality and delivery before you commit.
This website uses cookies to enhance your experience, remember your preferences, and help us understand how visitors use our site. You can accept all cookies, reject non-essential cookies, or manage your settings.
This website uses cookies to improve your experience while you navigate through the website. Out of these cookies, the cookies that are categorized as necessary are stored on your browser as they are essential for the working of basic functionalities of the website. We also use third-party cookies that help us analyze and understand how you use this website. These cookies will be stored in your browser only with your consent. You also have the option to opt-out of these cookies. But opting out of some of these cookies may have an effect on your browsing experience.
Necessary cookies are absolutely essential for the website to function properly. These cookies ensure basic functionalities and security features of the website, anonymously.
Cookie
Duration
Description
cookielawinfo-checkbox-analytics
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytics".
cookielawinfo-checkbox-functional
11 months
The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional".
cookielawinfo-checkbox-necessary
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Necessary".
cookielawinfo-checkbox-others
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Other.
cookielawinfo-checkbox-performance
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance".
viewed_cookie_policy
11 months
The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data.
Functional cookies help to perform certain functionalities like sharing the content of the website on social media platforms, collect feedbacks, and other third-party features.
Performance cookies are used to understand and analyze the key performance indexes of the website which helps in delivering a better user experience for the visitors.
Analytical cookies are used to understand how visitors interact with the website. These cookies help provide information on metrics the number of visitors, bounce rate, traffic source, etc.
Advertisement cookies are used to provide visitors with relevant ads and marketing campaigns. These cookies track visitors across websites and collect information to provide customized ads.