PCB manufacturing PCB manufacturing
Home > Blog

Counterbore: Symbols, Hole Dimensions and PCB Design

October 3rd, 2026

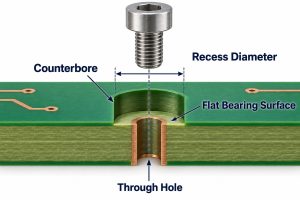
A counterbore is a cylindrical, flat-bottomed recess around a smaller hole. It provides space for a screw head, washer or other hardware to sit below the surrounding surface. A drawing must define the smaller hole diameter, recess diameter and recess depth; the screw thread size alone is not enough.

On a PCB, the recess also removes insulating material and may approach internal copper. The design therefore needs a remaining-thickness calculation as well as a fastener-fit check. A counterbore that fits a metal bracket can be too deep for the circuit board mounted beside it.
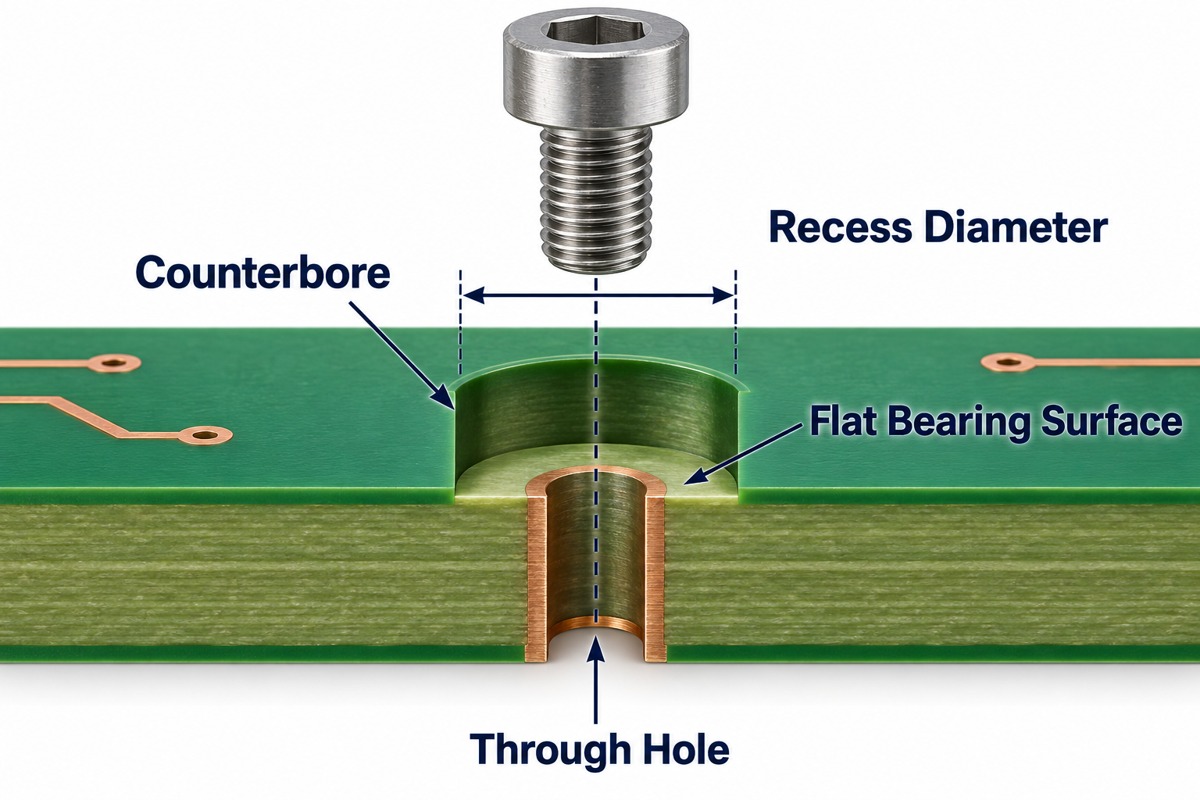
Cutaway showing a counterbore recess, flat bearing floor, through hole and socket-head screw

Key Takeaways

  • A counterbore has straight walls and a flat bearing floor; a countersink has a conical seat.
  • The ⌴ symbol identifies a counterbore. Diameter, depth, machining side and tolerances make the feature manufacturable.
  • Choose recess dimensions from the actual screw head and washer, not just the nominal thread size.
  • An ordinary M3 socket-head cap screw can have a 3 mm head height, so it cannot be fully recessed into a 1.6 mm PCB.
  • Check minimum board thickness minus maximum recess depth, then review the remaining structure and internal copper.
  • Copper clearance follows the full recess boundary, not only the smaller through hole.
  • Inspection should check diameter, depth, location, floor condition and hardware fit.

What Is a Counterbore Hole?

A counterbore hole is a stepped hole with a larger cylindrical opening above a smaller bore. The annular floor supports the underside of the fastener head or washer, while the smaller bore provides a path for the screw shank.

Feature Geometry Primary purpose
Counterbore Cylindrical recess with a flat floor Accommodate a cylindrical head or washer
Countersink Conical recess Seat a matching flat-head screw
Spotface Shallow machined flat seat Create a suitable bearing surface
Clearance hole Single-diameter bore Allow the screw shank to pass without thread engagement

The word also names the cutting tool used to make this recess. A request for a “counterbore” should therefore distinguish the finished feature from the tool. The smaller hole can be through or blind, although PCB mounting designs commonly use a through hole.

When Does a PCB Need a Counterbore?

A PCB needs a counterbore when hardware must sit below its surface and the board has enough material to retain a sound bearing floor. Examples include a recessed mounting screw near an enclosure wall or hardware that would otherwise interfere with a cover.

At EBest Circuit, we support counterbore-hole designs within our FR4 PCB fabrication services. Send the screw drawing and board stackup with the mechanical detail so we can review the machining side, remaining material and copper clearances before production.

Recessing a screw does not automatically make its joint stronger. Where the board is too thin, move the recess into the enclosure or mounting bracket, or use a suitable standoff. Our earlier article on counterbores in PCB design and manufacturing introduces related mounting applications.

Counterbore Symbol and Drawing Callout

The counterbore symbol is ⌴, placed before the recess diameter. A complete counterbore callout also identifies depth and the smaller hole, with units and tolerances supplied by the detail or drawing notes.

For example, an illustrative drawing could specify 4X Ø3.4 THRU; ⌴ Ø6.5, DEPTH 3.2; TOP SIDE; ALL DIMENSIONS IN mm. This describes four through holes, each with a larger top-side recess. It is a reading example, not an approved PCB design or a universal M3 standard.

  • 4X: four identical features.
  • Ø3.4 THRU: the smaller bore passes through the part.
  • ⌴ Ø6.5: the cylindrical recess is 6.5 mm in diameter.
  • DEPTH 3.2: the recess floor lies 3.2 mm below the specified top reference surface.
  • TOP SIDE: the feature is machined from the identified face.

Add dimensional tolerances, hole location and the intended plated or non-plated condition before releasing the drawing. A simple “M3 counterbore” note leaves the screw family, washer and recess geometry unresolved. If a font does not display ⌴ clearly, retain the section view and use an explicit COUNTERBORE note.
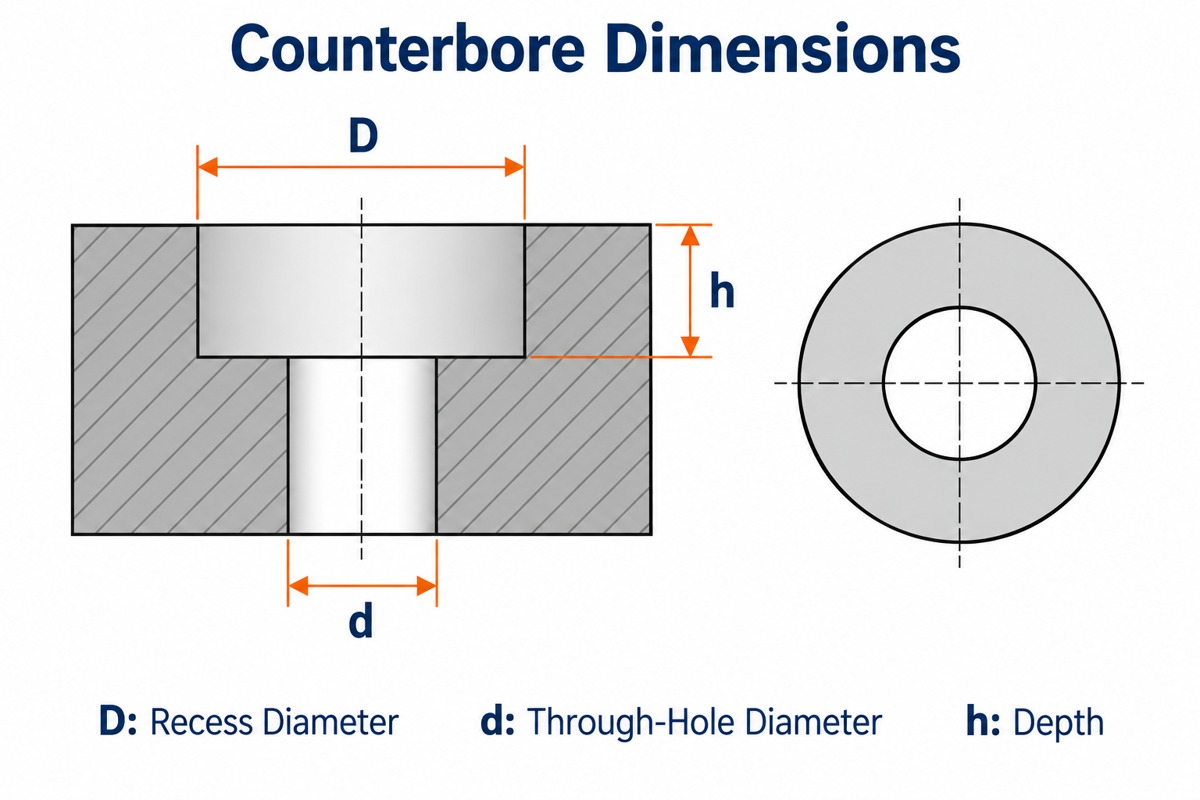
Section and top views identifying counterbore diameter D, through-hole diameter d and depth h

How Do You Choose Counterbore Diameter and Depth?

Choose the diameter to clear the maximum screw-head or washer diameter, and choose the depth to achieve the required installed head position. Check these dimensions against the purchased fastener drawing, including its tolerances.

A standard-height M3 socket-head cap screw commonly has a 5.5 mm head diameter and a 3 mm head height. These are fastener dimensions, not the finished recess dimensions. A low-head or button-head M3 screw has a different envelope, even though its thread is still M3.

  • Radial fit: the smallest permitted recess must clear the largest permitted head, allowing for positional error.
  • Axial fit: the shallowest permitted recess must accommodate the tallest head and any washer when full recessing is required.
  • Tool access: allow the driver or socket to reach the screw without hitting nearby components.
  • Corner fit: check the under-head fillet against the smaller hole edge and any specified edge break.

For an illustrative 6.5 mm recess and 5.5 mm head, nominal radial clearance is (6.5 − 5.5) ÷ 2 = 0.5 mm per side. Tolerances and offset reduce that clearance. Do not treat a nominal fit as a worst-case fit, or add a washer after approving the recess depth.

How Much PCB Thickness Must Remain Below the Recess?

The worst-case remaining thickness is the minimum finished board thickness minus the maximum recess depth. That result must still satisfy the mechanical load and electrical-isolation requirements of the actual stackup.

Remaining thickness = minimum finished thickness − maximum machined depth. There is no single remaining-thickness value that is safe for every laminate, fastener load and copper arrangement.

Illustrative input Value
Board thickness specification 3.20 ± 0.15 mm
Recess depth specification 1.00 ± 0.10 mm
Minimum finished thickness 3.05 mm
Maximum recess depth 1.10 mm
Worst-case remaining thickness 1.95 mm

These inputs demonstrate the calculation; they are not EBest Circuit capability limits or a released fastening design. The 1.95 mm result says how much material remains, not whether the joint passes its strength or insulation requirements.

A 3 mm-high screw head cannot be fully buried in a 1.6 mm board while retaining a floor. Increasing recess diameter does not solve this depth problem. Change the hardware or move the recessed feature to a thicker mechanical part.
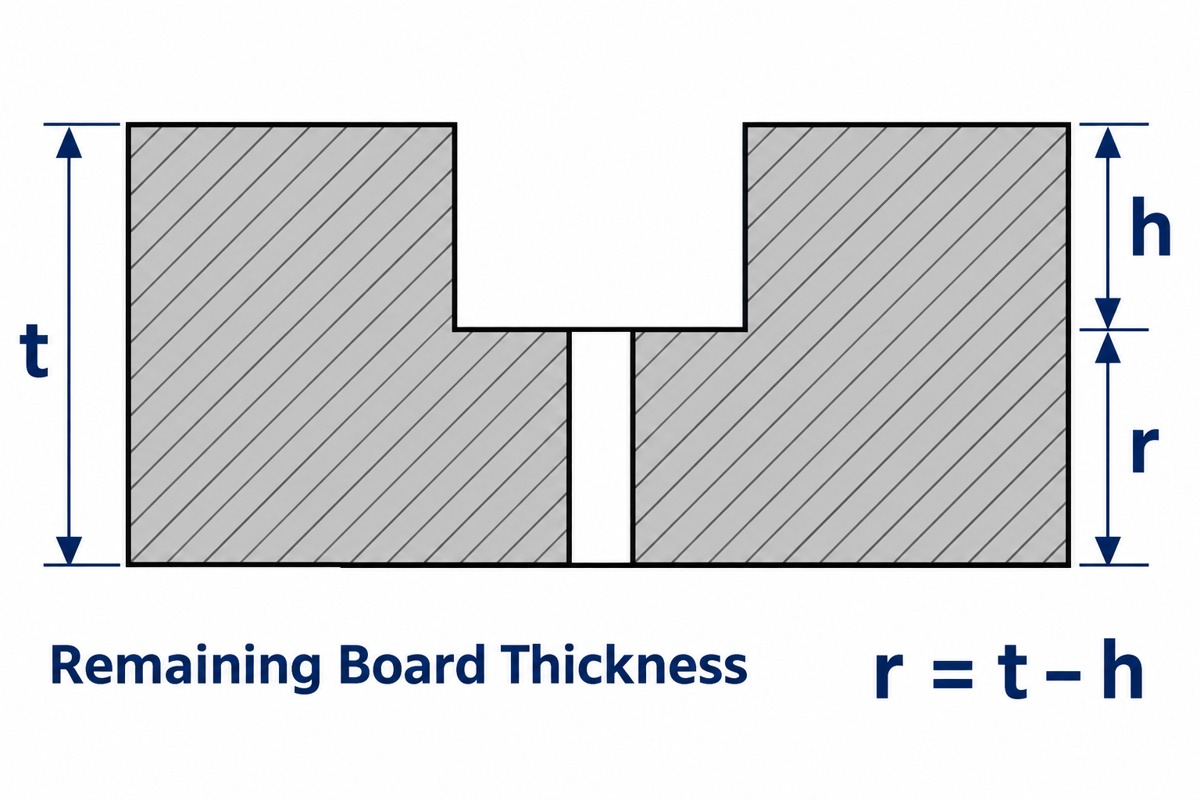
PCB section showing total thickness, recess depth and remaining material beneath the counterbore floor

How Should Copper Be Cleared Around a Counterbore?

Clear copper from the entire machined recess envelope on every layer the cut can reach, then add the project’s manufacturing and electrical clearance allowances. A keep-out around only the smaller through hole can leave copper exposed on the recess wall or floor.

Review the stackup in section, not just the top-layer layout. Include recess position and diameter tolerances, depth variation, internal-plane registration and the conductive hardware envelope. Solder mask should not be treated as the sole insulation between a clamped screw and a conductor.

  • Check internal planes as well as visible surface traces.
  • Define whether any copper contact is intentional for chassis grounding.
  • Keep nearby vias, pads and components outside the required machining and assembly envelope.
  • For metal-core boards, assess isolation from the exposed metal base separately.

The final clearance belongs in the approved design rules and fabrication drawing. Our PCB design guidance provides the broader design context; the recessed mounting detail still needs a project-specific stackup review.
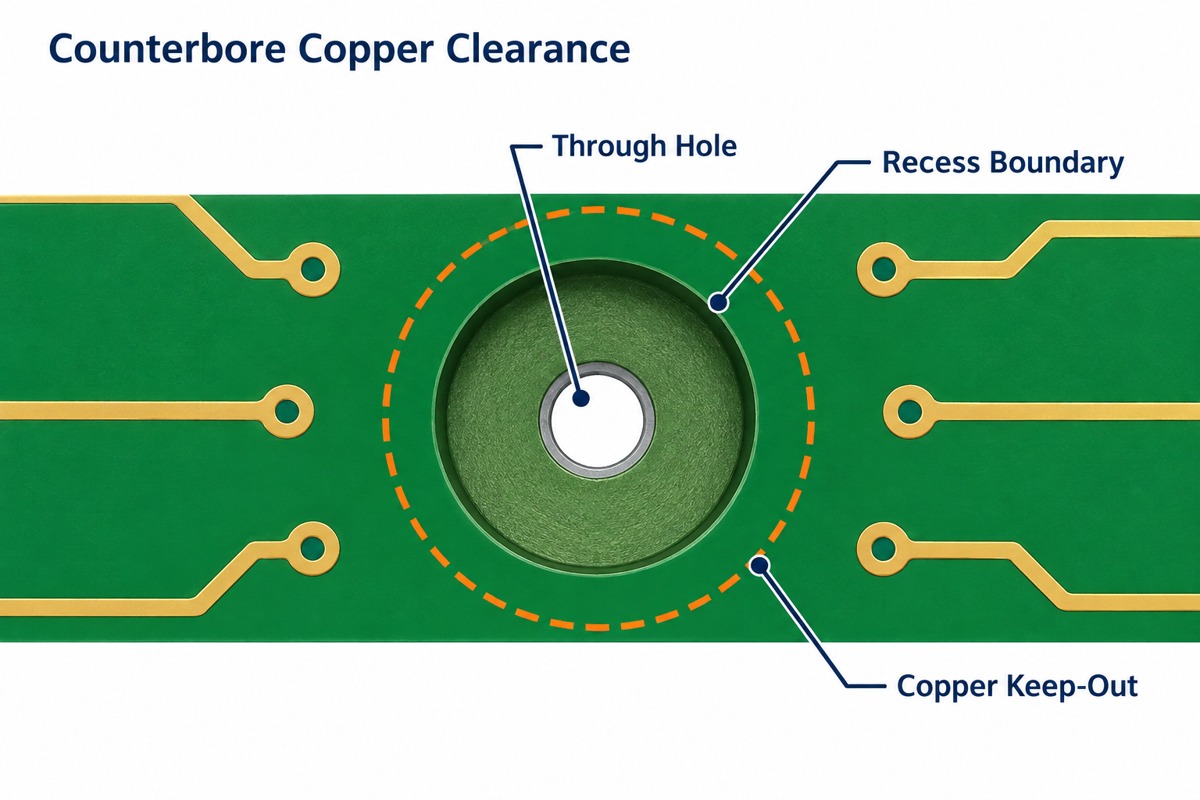
Top view showing copper clearance outside the full counterbore recess rather than only the smaller hole

Which Counterbore Tool Creates a Flat Bottom?

A purpose-made counterbore cutter or a suitable flat-bottom milling tool can form the recess. An ordinary pointed twist drill leaves a conical bottom and does not create the required flat annular bearing seat by itself.

A piloted counterbore tool uses the smaller hole to guide the cutter. CNC milling can instead locate the recess from the board’s reference system. Tool choice depends on material, diameter, depth, access and the required floor finish; metalworking speed-and-feed charts should not be copied directly to glass-reinforced PCB laminate.

For FR4, the process must address abrasive glass reinforcement, breakout and dust extraction. The fabrication drawing should specify the finished geometry and acceptance requirements, while the manufacturer selects a qualified machining method.

How Are Counterbores Made in PCBs?

PCB counterbores are made by controlled-depth machining at the specified hole locations, followed by cleaning and dimensional inspection. The fabricator determines the operation sequence relative to drilling, plating and other board processes.

  1. Review the detail: reconcile the mechanical drawing, stackup, drill data and fastener envelope.
  2. Establish the reference: identify the machining side, depth datum and location datum.
  3. Support the board: fixture the part so cutting loads do not bend or damage it.
  4. Machine the feature: control the larger recess diameter and floor depth using the approved toolpath.
  5. Clean and inspect: remove debris, check edges and measure the finished feature.

If the smaller bore must be plated, specify that requirement independently from the recess surfaces. Machining after plating can remove copper in the cut area; a drawing that merely says “plated hole” does not define the finished condition of every exposed surface.

What Should Counterbore Inspection Check?

Inspection should verify recess diameter, depth, location and floor condition, then confirm that the specified hardware seats correctly. A screw fitting into the hole does not prove that sufficient laminate or copper clearance remains.

Feature Inspection approach
Diameter and relative position Optical or dimensional measurement against drawing datums
Recess depth Depth measurement from the specified surface to the annular floor
Floor and edges Magnified inspection for burrs, raised fibers, damage and uneven seating
Fastener fit Specified screw and washer checked for interference and installed height
Hidden layer relationship Stackup review; agreed sectioning or additional verification where needed

A depth-gauge probe must contact the recess floor, not fall into the central through hole. Agree the measurement method before production when the annular seat is narrow or the top surface has features that affect the reference.
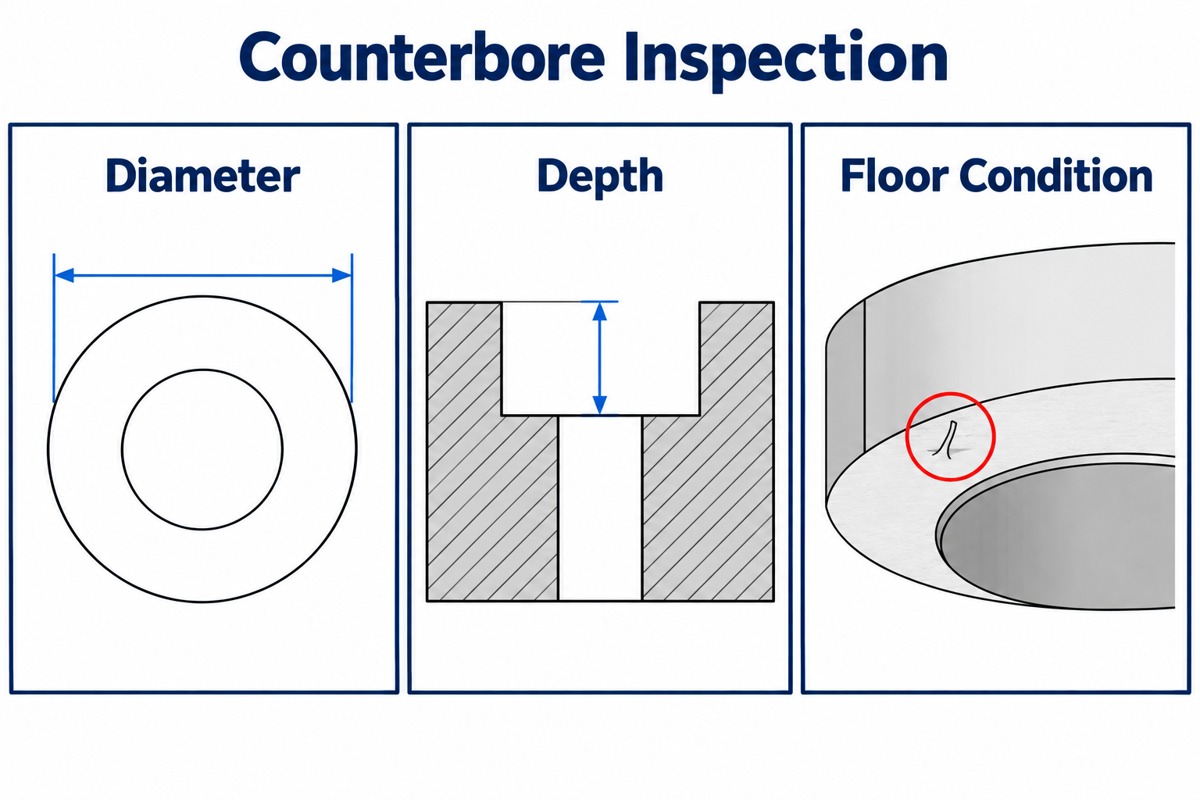
Counterbore inspection concepts showing diameter measurement, recess depth and floor condition

What Causes Counterbore Assembly Problems?

Incorrect depth, insufficient diameter, hole offset and damaged bearing surfaces are common causes of poor seating. Identify the physical interference before enlarging or deepening the recess.

  • Head stands proud: check actual head height, washer thickness and shallowest recess depth.
  • Screw enters but will not seat: check the under-head fillet, burrs and small-hole edge geometry.
  • Head rubs one side: check positional offset and minimum radial clearance.
  • Board cracks during tightening: review remaining thickness, backing support and the assembly torque specification.
  • Electrical contact appears after assembly: inspect exposed copper, metal-core contact and the hardware clearance envelope.

Do not correct a seating problem by tightening harder. Rework that changes recess depth or exposes a new layer needs engineering approval and renewed inspection.

When Is a Countersink or Spotface More Appropriate?

A countersink is appropriate for a matching conical flat-head screw; a spotface is appropriate when only a flat bearing surface is needed. Neither is a universal replacement for a counterbore in a thin PCB.

A countersink still removes material and must match the screw’s included angle. A spotface normally leaves the head above the surrounding surface, so it will not solve a requirement for full head recessing. For a wider comparison of the hole types and hardware, see our counterbore vs countersink guide.

FAQ About Counterbores

Does counterbore depth include the through hole?

No. It measures from the specified entry surface to the floor of the larger recess. Through-hole depth or the THRU designation is a separate requirement.

Is a counterbore hole threaded?

The enlarged recess normally provides clearance for hardware, not thread engagement. A smaller bore may be threaded in a mechanical component, but ordinary PCB mounting holes usually pass the screw to a nut, standoff or threaded enclosure.

Can the same counterbore fit every M3 screw?

No. M3 identifies the nominal thread diameter, not one head shape or height. Socket-head, low-head and button-head screws require different envelope checks. Washers can also change the required diameter and depth.

Is counterboring the same as backdrilling a PCB?

No. Counterboring creates a mechanical recess, usually for hardware. PCB backdrilling removes an unwanted plated via stub for electrical performance. Their purposes, depth targets and acceptance criteria are different.

Are Gerber files enough to specify a counterbore?

Not reliably on their own. Provide a dimensioned mechanical drawing with a section view, depth, machining side and tolerances, together with drill data and the stackup. Reconcile any differences between the drawing and manufacturing files before release.

Need a PCB Counterbore Reviewed Before Fabrication?

At EBest Circuit, we can review the recessed-hole detail alongside your FR4 board design and manufacturing files. Our PCB and PCB assembly services let you address fabrication geometry and final hardware access within the same project.

Send Gerber files, drill data, the board stackup, a dimensioned counterbore drawing, the screw or washer specification and quantities to sales@bestpcbs.com. Include any insulation, grounding or mechanical-load requirements so we can assess the feature before quoting.
You may also like

How an Orthogonal Backplane PCB Shortens Signal Paths

October 3rd, 2026

An orthogonal backplane PCB connects cards arranged at right angles, allowing high-speed signals to cross between them without long routes across a conventional backplane. This layout is used in networking and other modular electronic systems where board-to-board distance contributes to signal loss. Some designs retain a central PCB; direct orthogonal designs remove it from the high-speed connection.

EBest Circuit supports multilayer PCB fabrication, controlled-impedance construction, component sourcing and PCBA for customer designs. For an orthogonal backplane project, we can review the proposed board construction and assembly scope against your fabrication and connector requirements. Discuss your project with our team at sales@bestpcbs.com.

orthogonal backplane PCB

What Is an Orthogonal Backplane PCB?

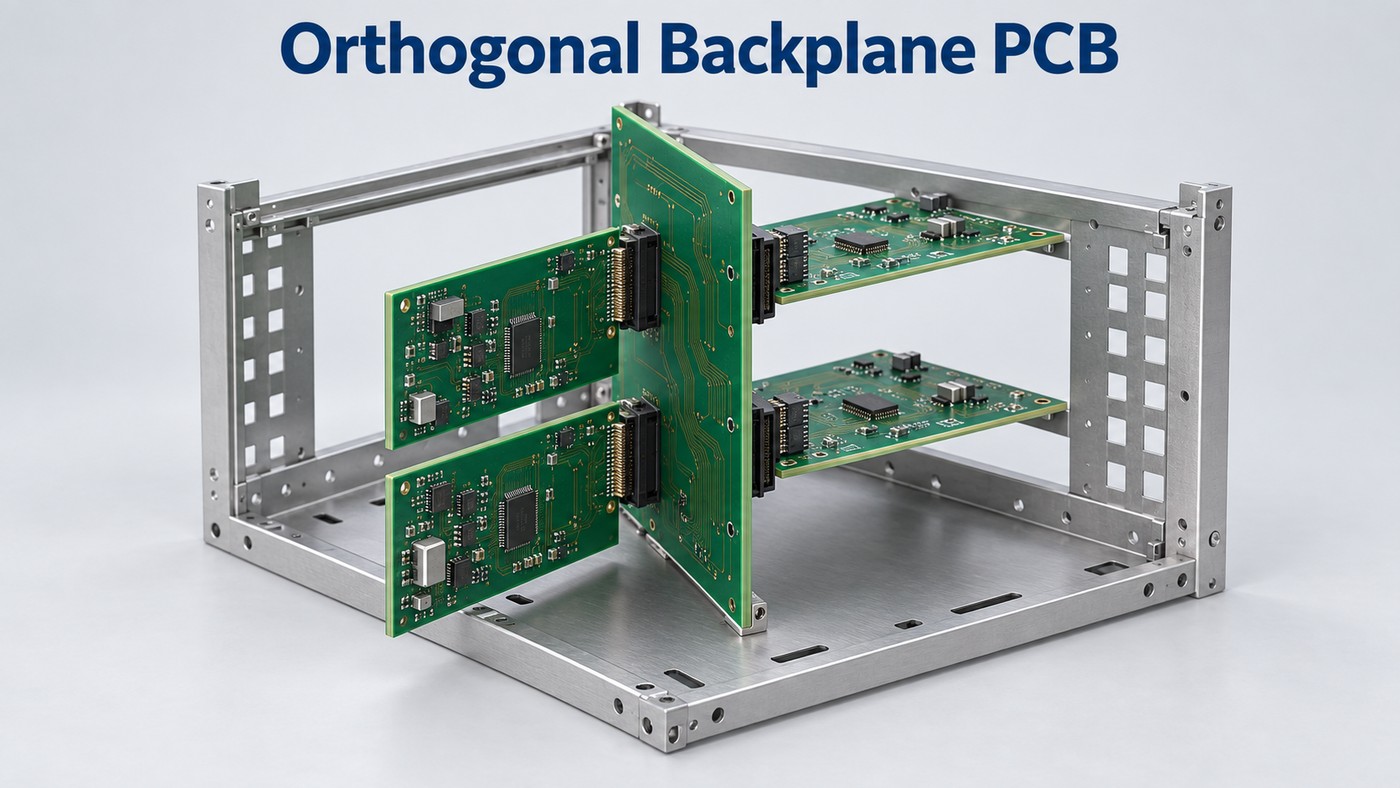
An orthogonal backplane PCB is part of an interconnect structure in which one group of plug-in cards sits perpendicular to another. In a typical arrangement, vertical cards enter from the front of a chassis and horizontal cards enter from the rear. Their connectors meet at the crossing points.

In a network switch, the two card groups may perform different jobs:

  • Line cards handle external network connections.
  • Switch fabric cards carry traffic between line cards inside the system.

Placing these cards across one another allows each line card to connect to several switch fabric cards near their intersections. A conventional backplane instead carries signals along PCB traces between card connectors distributed across the board.

The word “orthogonal” describes the relative orientation of the cards. It does not specify a layer count, laminate or data rate. It also does not tell you whether the assembly contains a midplane PCB, which is the central board between the two card groups.

How Do Orthogonal Midplane and Direct Orthogonal Connections Differ?

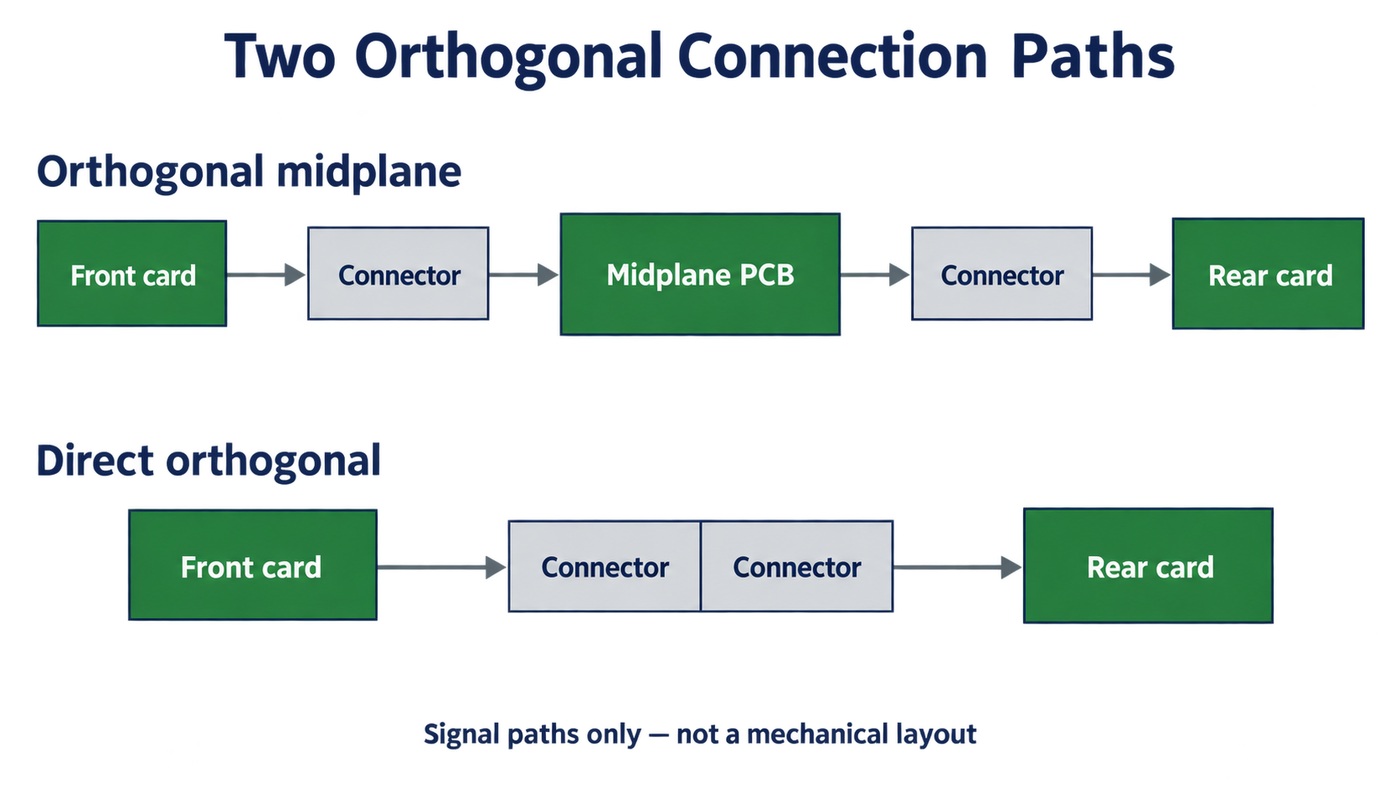
An orthogonal midplane retains a PCB between the cards. A direct orthogonal connection mates the perpendicular cards without that intermediate PCB in the high-speed path.

Feature Orthogonal midplane Direct orthogonal
Central PCB Remains between the card groups Removed from the direct signal connection
Signal crossing Passes through the midplane interconnect Passes through the mating card connectors
Connector mounting Opposing connectors attach to the midplane Connectors attach to the intersecting cards
Mechanical reference Midplane helps establish connector positions Chassis guides and card supports establish alignment

In one orthogonal midplane arrangement, connectors on opposite faces share signal and ground vias. The connection passes through the board instead of following a long lateral trace. Other power, management or inter-slot connections may still be routed within the midplane.

Direct orthogonal construction removes the intermediate board transition as well. However, it also removes the central mounting reference. Card guides, connector guidance features and the permitted movement between mating parts become more important because two separate cards must meet correctly inside the chassis.

“Backplane-free” therefore refers to the direct connection architecture. The system still contains PCBs and may use separate boards or cables for power and other functions.

orthogonal backplane PCB

How Does Orthogonal Backplane PCB Design Reduce Signal Loss?

Orthogonal backplane PCB design can reduce signal loss by shortening the distance a signal travels through PCB traces. A pass-through midplane replaces a long cross-board route with a short through-board connection. Direct orthogonal mating removes the intermediate PCB segment entirely.

The electrical benefit comes from the changed path:

  • Less trace length: the signal encounters less conductor and dielectric loss along the removed route.
  • A shorter central connection: a local pass-through avoids routing the same signal between distant backplane connectors.
  • Fewer intermediate board transitions in a direct design: the channel no longer includes the removed midplane’s connector-to-PCB transitions.

Shorter does not mean lossless. The remaining connector contacts, PCB launches and vias still influence impedance, reflections and crosstalk. A launch is the transition between the connector and the board’s transmission line; poor geometry there can consume part of the benefit gained from a shorter route.

The relevant comparison is the complete channel from transmitter to receiver. Reducing its length can improve the loss budget, but the right-angle card arrangement alone cannot establish a maximum data rate or a fixed percentage improvement.

How Does an Orthogonal Card Layout Change Airflow?

An orthogonal card layout changes where boards and connectors obstruct air inside the chassis. It can open a more direct cooling path, particularly when a large central backplane is removed, but rotating the cards by 90 degrees does not automatically improve cooling.

With a midplane, air moving between the front and rear compartments must pass through available openings or around the board. Connector fields and routed areas limit where those openings can be placed.

With direct orthogonal mating, the central PCB no longer forms the same barrier. Space between connector groups may allow air to move through the card intersection more freely.

The remaining hardware still matters. Horizontal cards, heatsinks and support rails can block or redirect airflow even without a midplane. A useful cooling layout must carry air past the hot components on both card groups, rather than simply provide an open space in the middle of the enclosure.

What Materials and Layer Counts Do Orthogonal Backplane PCBs Use?

Orthogonal backplane PCBs do not have a standard material or layer count. The construction depends on whether the board carries long routed channels, short pass-through connections, or a mixture of signal and power functions.

Board function Main influence on construction
Routed high-speed channels Dielectric loss, copper loss and controlled-impedance geometry
Short midplane pass-throughs Connector footprint, plated-hole geometry and reference connections
Power and management routing Current distribution, routing space and plane allocation

For long high-speed routes, low-loss laminates can preserve more of the channel’s signal budget. A short pass-through structure may reduce that material burden, but its suitability still depends on the operating frequency and the complete connection. Neither standard FR-4 nor a premium low-loss laminate is the automatic answer for every orthogonal system.

Layer count follows the routing that remains. Signals need space to escape dense connector fields, while ground references and power distribution occupy additional layers. Removing lateral signal routes can reduce routing demand, although connector density and other board functions may still require a substantial multilayer stackup.

There is no universal 78-layer requirement. A layer count quoted for one high-density platform describes that particular design, not the definition of an orthogonal backplane PCB. Adding layers without a routing or electrical purpose also increases board thickness and manufacturing complexity.

How Does Orthogonal Backplane PCB Thickness Affect Vias and Connectors?

Orthogonal backplane PCB thickness affects both the distance signals travel through plated holes and the way connector pins engage those holes. A thicker board may provide useful stiffness, but its electrical and connector geometry must work together.

A through-board connection uses the via barrel.

When opposing connectors share a via through a midplane, the conductive barrel forms part of the intended signal path. That active section cannot be treated as unwanted copper simply because it passes through a thick board.

An unused via section is a different problem.

If a signal leaves a through-hole via on an inner layer, the barrel continuing beyond that connection can form a stub. At high frequencies, this unused branch can cause reflections and resonances. Backdrilling can remove the unwanted section where the design permits it, while retaining the required electrical connection and connector engagement.

Connector pins require a compatible board construction.

Press-fit contacts have defined compliant sections that engage plated holes. Board thickness, finished-hole size and the connector’s specified mounting geometry determine whether that engagement is correct. In a two-sided midplane, the opposing contacts and their insertion depths must also fit the intended shared-hole arrangement.

Board thickness is therefore tied to the selected interconnect. Increasing it for stiffness, or removing barrel copper for signal integrity, can change the same structure that holds and connects the pins.

How Are Connectors Mounted in Orthogonal Backplane PCB Assembly?

Connectors in orthogonal backplane PCB assembly may use press-fit or soldered termination, depending on the connector family. “Orthogonal” describes how the cards meet; it does not define how a connector attaches to its PCB.

Press-fit mounting

A compliant pin compresses as it enters a specified plated hole. The resulting contact provides electrical connection and mechanical retention without a solder joint at that interface.

For a dense connector array, the board is supported close to the insertion area and a suitable tool applies force through the connector’s intended pressing surfaces. This helps prevent board bending, bent pins and damage to the plated holes. Correct seating across the connector matters because an unevenly installed housing can misalign the mating interface.

Soldered mounting

Solder-terminated connectors require the assembly process specified for their mounting style. Surface-mount contacts use an appropriate reflow process; through-hole contacts use a suitable through-hole soldering process. Connector materials, board thermal mass and access to the joints influence the assembly method.

Card mating after assembly

Installing a connector on a PCB and plugging two cards together are separate operations. A connector can be securely attached to its board yet still meet the opposite card at the wrong position or angle. Chassis guides and connector alignment features help the mating contacts engage as intended without forcing the cards sideways.

Post-assembly inspection can identify seating and pin problems, while electrical testing can detect connection faults. Neither result alone demonstrates that the complete link meets its high-speed performance target.

orthogonal backplane PCB

FAQs About Orthogonal Backplane PCB

1. Is an orthogonal backplane PCB the same as orthogonal PCB routing?

No. An orthogonal backplane connects perpendicular cards. Orthogonal routing usually refers to traces running in different directions on adjacent PCB layers. The terms describe different levels of the design.

2. Are orthogonal backplanes used only in AI servers?

No. Orthogonal interconnects are also used in network switches, routers and other modular systems. Their relevance comes from the card arrangement and board-to-board connection distance, rather than an AI-specific function.

3. Is an orthogonal backplane always passive?

No. A midplane may provide passive interconnections, while another implementation may include power or management circuitry. Orthogonal card orientation does not determine whether active components are present.

4. Can a standard right-angle board-to-board connector replace an orthogonal connector?

Not automatically. A connector that turns a connection through 90 degrees may have a different mating geometry, pin assignment, electrical performance or alignment allowance. The angle alone does not make the connectors interchangeable.

5. Does passing a continuity test confirm high-speed signal performance?

No. Continuity testing checks electrical connections for faults such as opens and shorts. High-speed channel performance also depends on loss, impedance discontinuities and crosstalk, which require suitable analysis or measurements beyond a continuity test.

Planning an orthogonal backplane PCB or its mating card assemblies? Send your proposed stackup and connector details to sales@bestpcbs.com. EBest Circuit can discuss PCB fabrication and assembly options for your design, including impedance-controlled construction and the scope of production inspection and testing.
You may also like

EMIB Technology: Structure, Process, Benefits & CoWoS

October 2nd, 2026

EMIB, or Embedded Multi-die Interconnect Bridge, is a 2.5D packaging technology that connects neighboring dies through small silicon bridges embedded inside the package substrate. Instead of placing an entire multi-die assembly on a large silicon interposer, EMIB concentrates fine-pitch routing only where high-bandwidth connections are required.

This localized architecture is well suited to chiplet processors, AI accelerators, HPC devices, FPGAs, and logic-plus-HBM packages. It combines the routing density of silicon at critical die interfaces with the larger routing area, power distribution, and mechanical support provided by an organic package substrate.

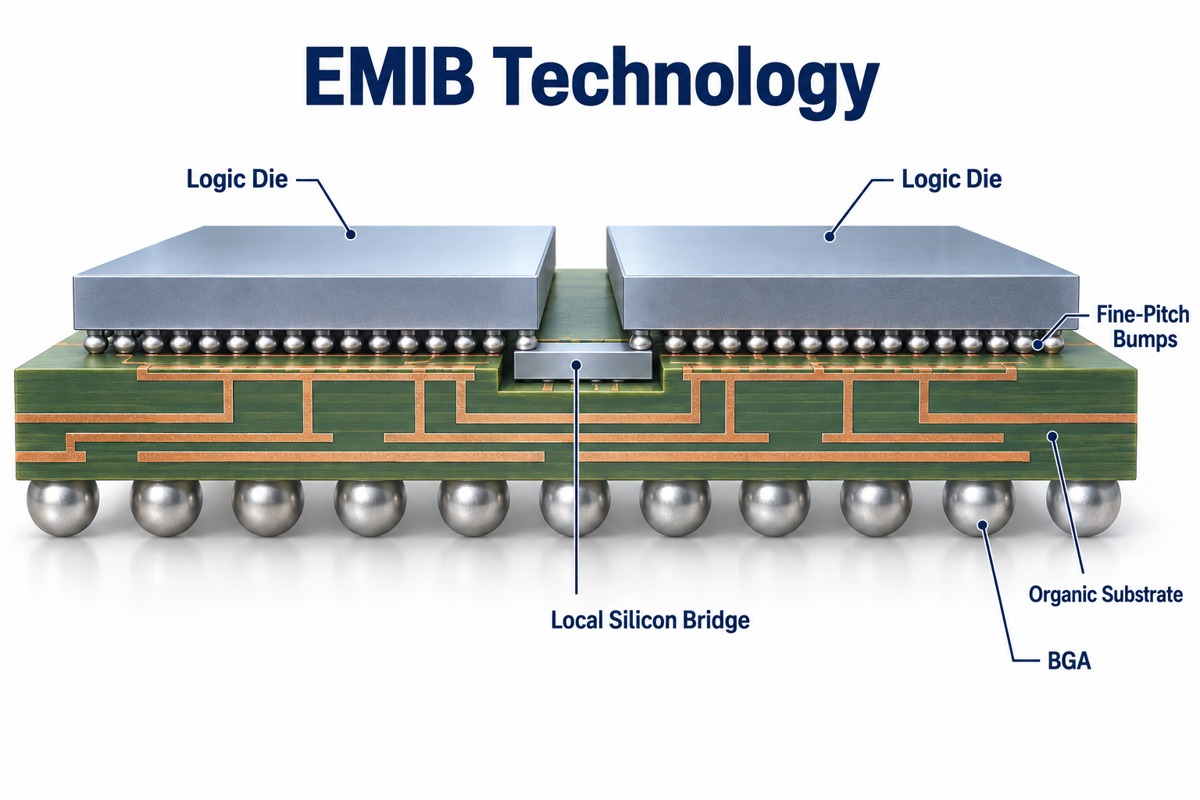
Conceptual EMIB package showing local silicon bridge, logic dies, substrate and BGA connections

Key Takeaways

  • EMIB stands for Embedded Multi-die Interconnect Bridge, a 2.5D packaging technology that places small silicon bridges inside the package substrate for high-density die-to-die connections.
  • Unlike a large silicon interposer, EMIB uses silicon only at selected interfaces where fine-pitch routing is required.
  • The silicon bridge connects adjacent logic dies, chiplets, or HBM through short, dense interconnects while the surrounding package substrate handles broader routing and power distribution.
  • EMIB manufacturing combines silicon bridge fabrication with cavity formation, bridge embedding, substrate build-up, fine routing, die attach, and package testing.
  • EMIB, EMIB-M, and EMIB-T share the localized bridge concept but add different electrical capabilities, including integrated capacitors or TSV-enabled vertical connections.
  • EMIB and CoWoS-L both use localized silicon interconnect structures, although their surrounding routing media and overall package architectures differ.

What Is EMIB?

EMIB is a localized silicon-bridge packaging architecture that provides high-density electrical connections between adjacent dies. A small piece of silicon with fine metal routing is embedded in the package substrate beneath the edges of two neighboring dies.

Fine-pitch bumps connect both dies to this silicon bridge. Signals can then cross the die boundary through short, dense routing without requiring a large silicon interposer underneath the complete package.

A typical EMIB package can include:

  • logic dies or compute chiplets;
  • HBM stacks;
  • one or more embedded silicon bridges;
  • fine-pitch die-to-bridge connections;
  • an organic package substrate;
  • copper power and signal routing;
  • BGA connections to the system PCB.

The bridge is used where routing density is highest. Lower-density signals, power, ground, and package-level connections can remain in the surrounding substrate, allowing different parts of the package to use interconnect structures suited to their actual electrical requirements.

What Is an EMIB Substrate?

An EMIB substrate is a package substrate containing one or more embedded silicon bridges beneath selected die interfaces. It still performs the normal functions of an advanced IC package substrate, but adds localized regions capable of much finer routing.
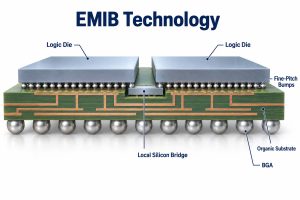
The main structures include:

Structure Main Function
Organic package substrate Broad signal routing, power distribution, and mechanical support
Embedded silicon bridge High-density die-to-die routing
Build-up layers Connect the bridge to surrounding substrate routing
Fine-pitch bumps Connect dies to the bridge
Copper vias and planes Carry power, ground, and package-level signals
BGA solder balls Connect the package to the system PCB

The key feature is localization. Only the interfaces that need very high routing density use silicon, while the rest of the package can rely on organic build-up technology.

This is useful in heterogeneous packages because routing requirements are rarely uniform. A compute die may need thousands of closely spaced connections to HBM, while other interfaces can operate with much wider routing pitches.

How Does EMIB Work?

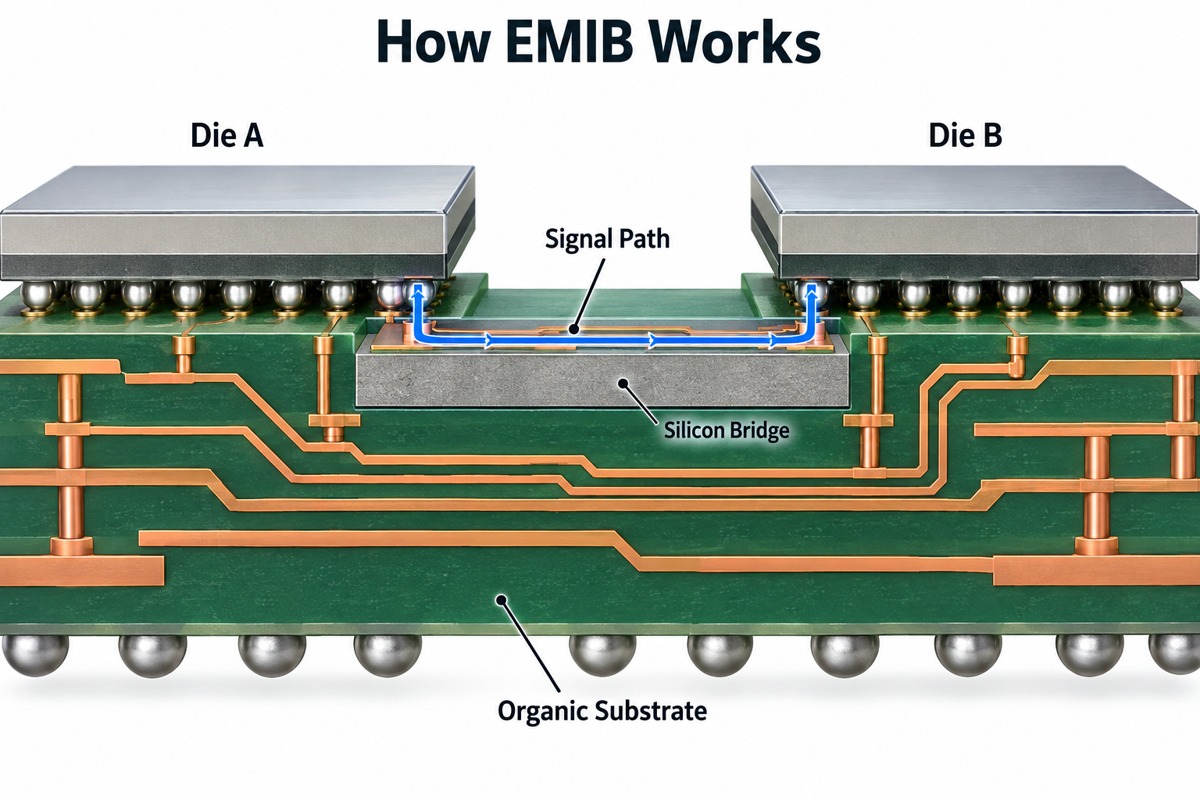
EMIB works by routing high-speed signals through an embedded silicon bridge positioned directly below the edges of neighboring dies. Fine-pitch bumps connect each die to the bridge, and the bridge’s metal layers carry signals across the gap.

The signal path can be simplified as:

  • Die A → Fine-Pitch Bumps → Silicon Bridge
  • Silicon Bridge → Fine-Pitch Bumps → Die B

This architecture is suitable for several high-bandwidth connections, including:

  • logic-to-logic;
  • compute-to-I/O;
  • logic-to-HBM;
  • accelerator-to-memory;
  • chiplet-to-chiplet interfaces.

The surrounding organic substrate does not need to match the bridge’s routing density. It can handle broader signal paths, power distribution, and connections toward the BGA, which keeps the high-density silicon region focused on the die boundaries where it provides the greatest value.

Signal routing between adjacent dies through a local silicon bridge

Why Does EMIB Use a Local Silicon Bridge?

EMIB uses a local silicon bridge because high-density routing is usually required only at specific die interfaces rather than across the entire package. A localized bridge places silicon exactly where the fine-pitch interconnect is needed.

This architecture provides several practical benefits:

  • silicon area is concentrated at critical interfaces;
  • neighboring dies communicate through short electrical paths;
  • organic routing remains available across most of the package;
  • bridge placement can follow the actual chiplet floorplan;
  • several bridges can be distributed across a large package;
  • package size can grow without requiring one equally large silicon interposer.

For example, a package containing multiple compute chiplets and HBM stacks may need very dense routing only between each logic die and its neighboring memory. Local bridges allow those interfaces to use silicon-level routing while the rest of the substrate remains optimized for package-scale connections.

What Is the EMIB Process Flow?

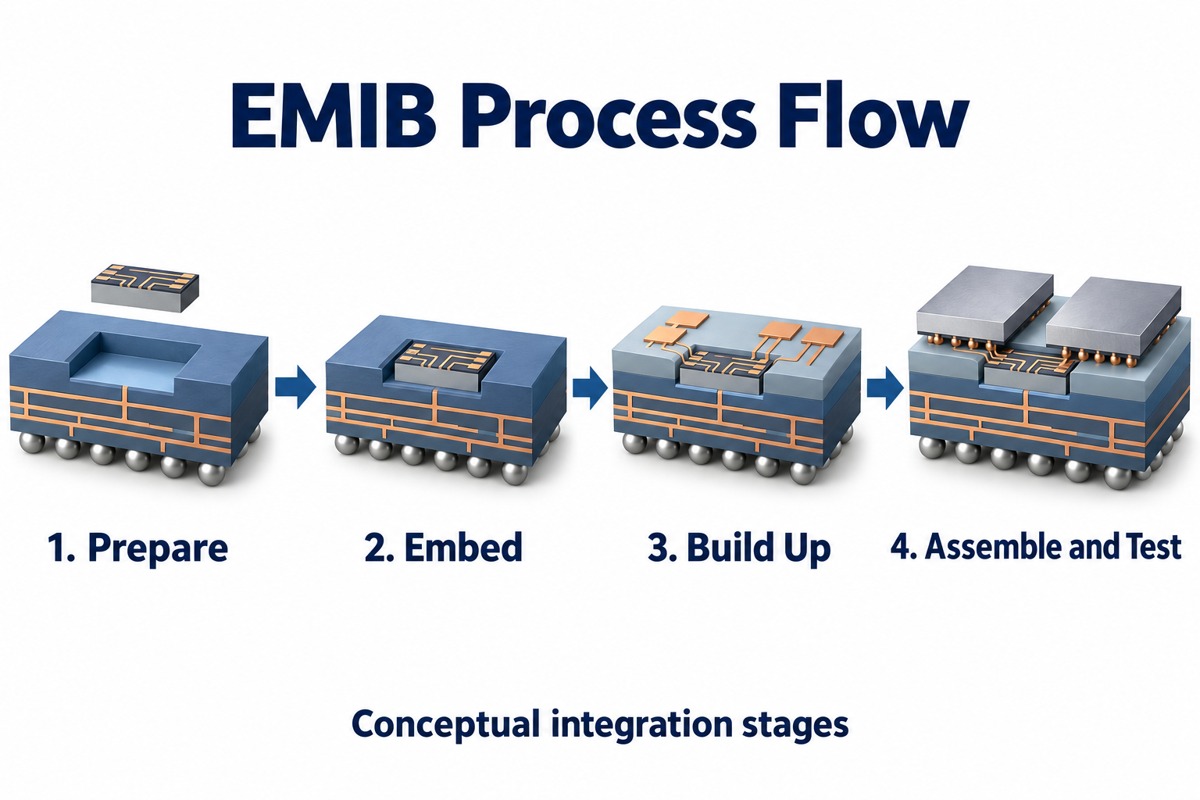
The EMIB process flow combines silicon bridge fabrication, substrate cavity preparation, bridge embedding, build-up routing, and final multi-die assembly. Exact production details depend on the package generation, but the general manufacturing sequence follows the same structure.

  1. Silicon bridge fabrication Fine metal routing is fabricated on the silicon bridge using semiconductor-compatible processing.
  2. Substrate cavity formation A recessed region is prepared at the location where the bridge will be embedded.
  3. Bridge placement The silicon bridge is accurately positioned inside the package substrate.
  4. Dielectric build-up Organic dielectric layers are formed around and above the embedded bridge.
  5. Copper routing formation Copper traces and vias connect the bridge region with the broader substrate routing.
  6. Fine-pitch interface preparation Pads and bump structures are prepared above the bridge for die attachment.
  7. Die attach Logic dies, chiplets, HBM, or other components are mounted on the substrate.
  8. Package assembly and test Underfill, mechanical reinforcement, electrical inspection, and reliability testing complete the package.

Bridge alignment is especially important because the embedded structure has to register with both the substrate routing below and the fine-pitch die connections above. Smaller interconnect pitches reduce the available margin for dimensional variation.

Four conceptual EMIB integration stages from cavity preparation to assembly and testing

What Are the Main Advantages of EMIB?

The main advantage of EMIB is that it provides silicon-level routing density without requiring a package-wide silicon interposer. This makes the architecture attractive when only selected interfaces need extremely dense connections.

Key advantages include:

  • High interconnect density: fine silicon routing supports wide die-to-die interfaces.
  • Short signal paths: adjacent dies communicate through compact local bridges.
  • Localized silicon usage: silicon is used mainly where its routing capability is required.
  • Heterogeneous integration: logic, memory, I/O, and accelerator dies can share one package.
  • Flexible floorplanning: bridge locations can follow chiplet placement.
  • Package scalability: multiple bridge regions can be distributed across a larger package.
  • Process-node flexibility: individual dies can use fabrication nodes suited to their functions.

This is particularly useful for chiplet architectures. Compute logic can use an advanced node, while I/O, analog, or supporting functions can use other processes without giving up high-bandwidth die-to-die communication.

What Are the Main EMIB Design and Manufacturing Challenges?

EMIB manufacturing must integrate fine-feature silicon structures into a much larger organic substrate while maintaining alignment, planarity, electrical performance, and long-term reliability.

The main challenges include:

  • Bridge placement accuracy: the silicon bridge must align precisely with fine-pitch die interfaces.
  • Substrate warpage: silicon, copper, dielectric, and molding materials expand differently during thermal cycling.
  • Coplanarity: uneven surfaces can affect die attach and fine-pitch joint quality.
  • Microbump reliability: small joints experience thermal and mechanical stress during assembly and operation.
  • Signal integrity: impedance, crosstalk, return paths, and interconnect discontinuities require careful control.
  • Thermal-mechanical stress: large logic dies and HBM stacks can create strong temperature gradients.
  • Yield management: a late-stage defect may affect several expensive known-good dies in the same package.

These issues become more difficult as package size increases. Larger substrates have tighter requirements for dimensional stability because even small material movement can affect bridge registration and fine-pitch assembly across the package.

EMIB vs Silicon Interposer: What Is the Difference?

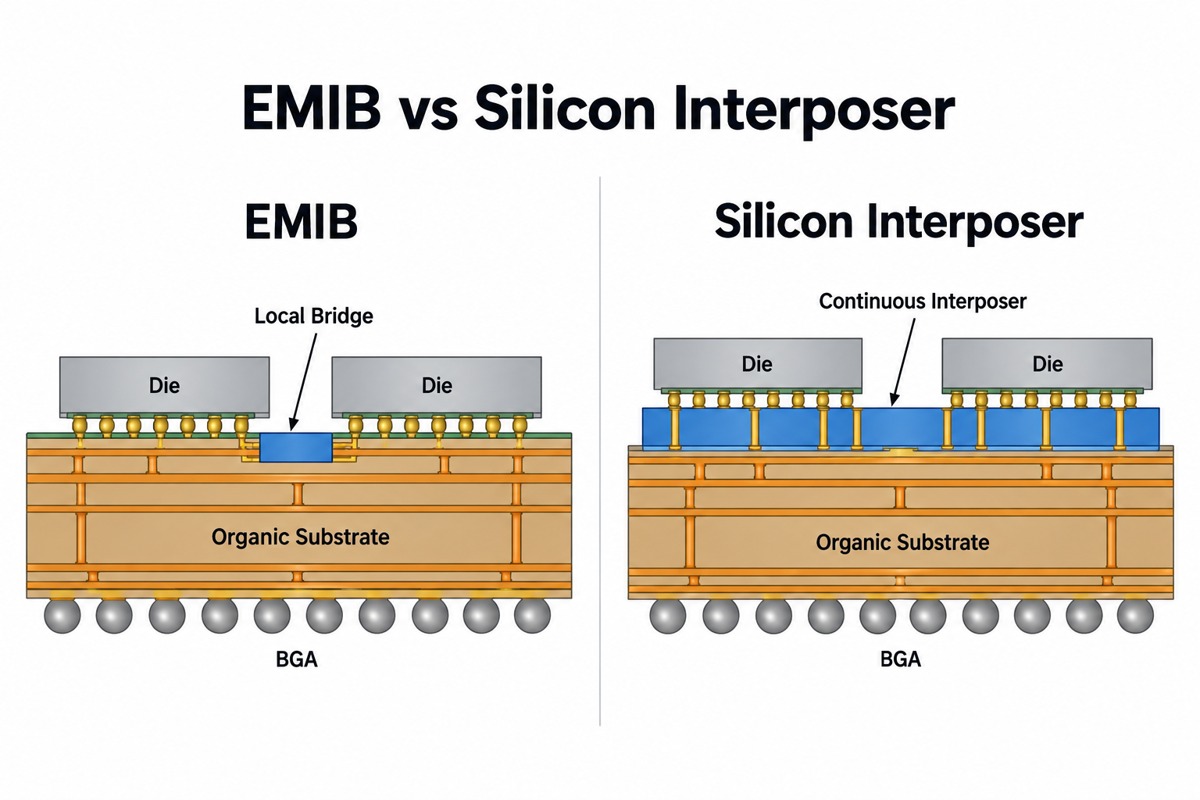
EMIB uses small localized silicon bridges, while a conventional silicon-interposer package uses a much larger continuous silicon routing layer beneath multiple dies. Both provide fine-pitch interconnection, but they distribute the high-density silicon very differently.

Feature EMIB Silicon Interposer
Silicon routing area Local bridge regions Large continuous area
Position Embedded in package substrate Beneath multiple dies
Fine routing coverage Selected die interfaces Broad interposer area
Package-level routing Mainly organic substrate Interposer + substrate
Conventional bridge TSVs Not required Common in silicon interposers
Scaling approach Add localized bridges Increase interposer area

A full silicon interposer is useful when dense routing is required across a broad die complex. EMIB is more localized, making it suitable when the highest routing density is concentrated along specific die boundaries.

The appropriate architecture depends on the package floorplan, number of dies, HBM placement, routing density, power distribution, thermal behavior, assembly requirements, and manufacturing economics.

Comparison of a local EMIB bridge and a continuous silicon interposer

EMIB vs CoWoS-L: How Do the Architectures Differ?

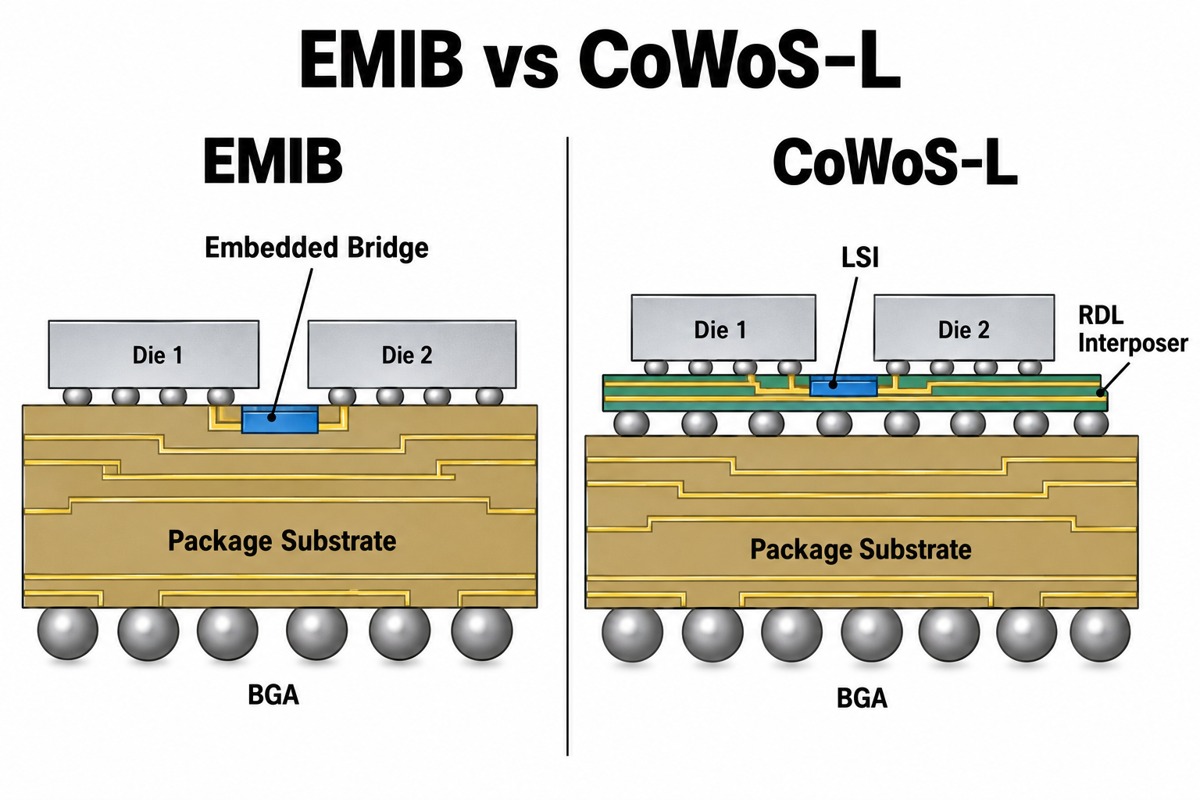
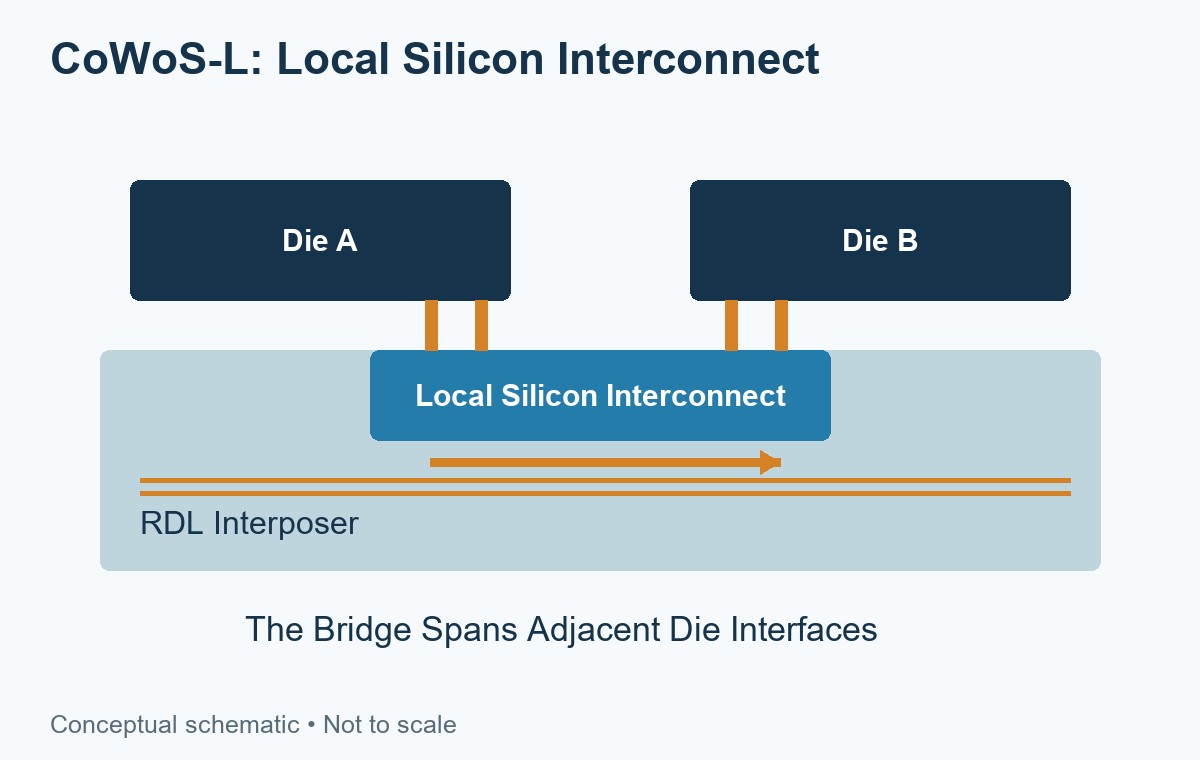
EMIB embeds localized silicon bridges directly inside the package substrate, while CoWoS-L uses local silicon interconnect structures within a broader RDL-based interposer architecture. Both use localized silicon for dense connections, but the surrounding routing structures are different.

Feature EMIB CoWoS-L
Local silicon structure Embedded silicon bridge Local Silicon Interconnect
Surrounding routing medium Package substrate RDL interposer
Fine-pitch routing Localized Localized
HBM integration Supported Supported
Package scaling Multiple bridge regions Larger RDL interposer with local silicon
Broader routing Organic build-up layers RDL structure

In an EMIB package, the organic substrate performs much of the broader routing around each silicon bridge. In CoWoS-L, the localized silicon structures are part of a larger redistribution-layer interposer system.

A practical comparison should consider more than the presence of a bridge. Engineers also need to evaluate:

  • die and HBM placement;
  • routing density;
  • package dimensions;
  • power distribution;
  • warpage;
  • thermal behavior;
  • assembly flow;
  • yield;
  • overall package cost.

These architectural differences become increasingly important as AI and HPC packages integrate more compute silicon and memory within the same package footprint.

EMIB substrate bridge compared with the distinct RDL and local silicon interconnect architecture of CoWoS-L

EMIB, EMIB-M and EMIB-T: What Is the Difference?

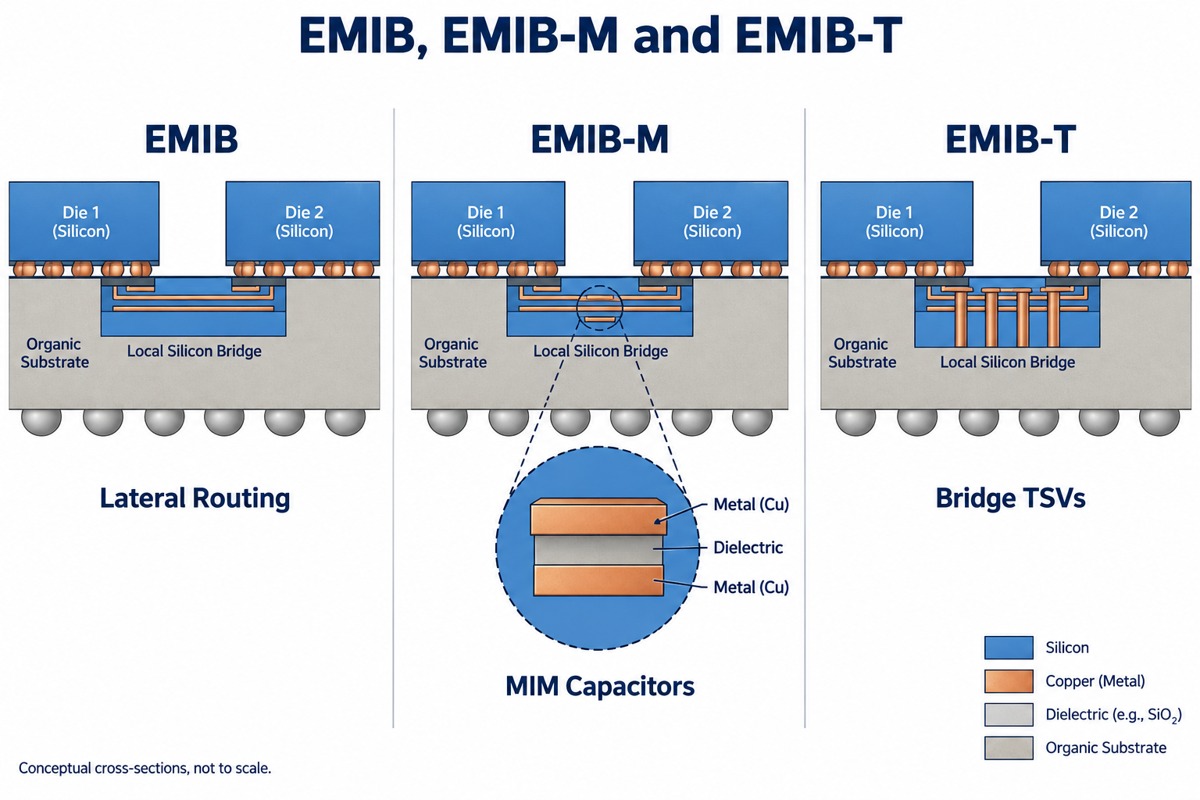
EMIB, EMIB-M, and EMIB-T share the same localized silicon-bridge concept, but the newer variants add specific electrical functions. Standard EMIB focuses mainly on lateral routing, while EMIB-M and EMIB-T expand the role of the bridge.

Technology Main Addition Primary Function
EMIB Local silicon bridge Fine-pitch lateral die-to-die routing
EMIB-M Integrated MIM capacitance Local decoupling and power support
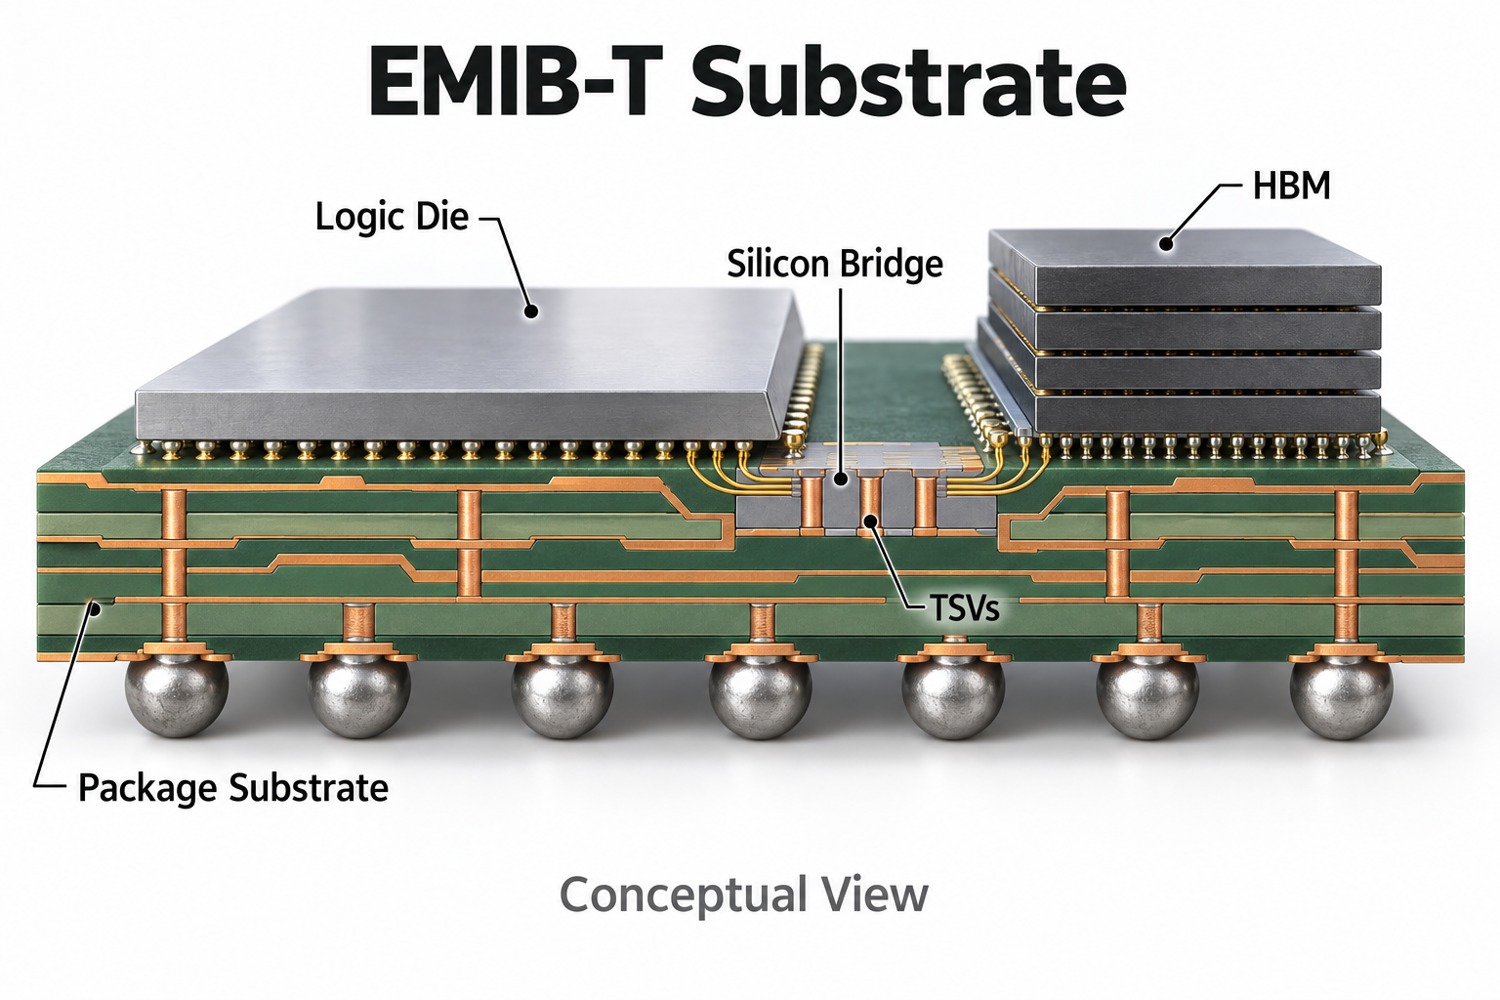
EMIB-T TSVs through the bridge Vertical electrical and power paths

EMIB-M integrates metal-insulator-metal capacitance close to the dies, which can support local power delivery and decoupling. EMIB-T adds through-silicon vias, allowing selected electrical paths to move vertically through the bridge.
The distinction is especially relevant for newer AI and HBM packages. As current demand increases, the bridge can evolve from a primarily signal-routing structure into a more active part of the package power-delivery architecture.

Comparison of conventional EMIB routing, EMIB-M capacitors and EMIB-T bridge TSVs

How Does EMIB Connect Chiplets, HBM and UCIe?

EMIB provides the physical high-density connection between neighboring chiplets or between logic and HBM. The silicon bridge carries the electrical signals, while standards such as UCIe define how compatible chiplets communicate at the interface level.

Typical EMIB connections include:

  • compute die to compute die;
  • compute die to I/O die;
  • compute die to HBM;
  • accelerator to accelerator;
  • UCIe-compatible chiplet links.

HBM is a strong use case because its wide interface benefits from short routing distances and high connection density. Chiplet interfaces have similar requirements when several dies need to exchange large volumes of data within the same package.

UCIe and EMIB therefore address different layers of the connection. UCIe defines the die-to-die interface framework, while EMIB can provide the physical package interconnect that carries those signals between adjacent dies.

Where Is EMIB Used in AI and HPC Packaging?

EMIB is used in advanced packages where multiple high-performance dies, memory stacks, or specialized chiplets require dense local interconnections. These applications increasingly depend on package-level bandwidth as much as on transistor performance.

Common application areas include:

  • AI training accelerators;
  • AI inference processors;
  • HPC processors;
  • data-center CPUs;
  • FPGAs;
  • multi-die GPUs and XPUs;
  • chiplet-based compute platforms;
  • logic-plus-HBM packages.

Heterogeneous integration also allows each die to use a manufacturing process suited to its function. Compute cores can use an advanced node, while I/O, analog, or supporting logic can remain on nodes better suited to cost, voltage, or interface requirements.

This approach helps designers scale system performance without increasing every function inside one extremely large monolithic die.

Can EMIB Use a Glass-Core Substrate?

EMIB can potentially be integrated with glass-core substrate platforms as advanced packages move toward larger dimensions and tighter registration requirements. Conventional EMIB, however, should still be understood as an embedded silicon-bridge architecture rather than a technology defined by glass substrates.

Glass-core substrates are being explored because they can offer useful properties for very large advanced packages:

  • improved dimensional stability;
  • lower warpage potential;
  • support for larger package formats;
  • finer routing capability;
  • stable electrical characteristics;
  • support for dense vertical and lateral interconnects.

Glass also introduces manufacturing challenges, including via formation, metallization, substrate handling, bonding, and integration with organic build-up layers. These processes must meet the same reliability and production requirements expected from established package-substrate platforms.

For future EMIB scaling, improved substrate stability could become increasingly valuable as packages integrate more silicon bridges, chiplets, and HBM stacks while maintaining tight alignment across a larger area.

EMIB FAQs

1. What does EMIB stand for?

EMIB stands for Embedded Multi-die Interconnect Bridge. It uses small silicon bridges embedded inside a package substrate to create fine-pitch connections between neighboring dies.

2. Is EMIB a 2.5D packaging technology?

Yes. EMIB is generally classified as a 2.5D heterogeneous integration technology because multiple dies are placed side by side and connected through localized high-density silicon interconnects.

3. Does EMIB use TSVs?

Conventional EMIB bridges do not require TSVs for their primary lateral die-to-die connection. EMIB-T is the variant that adds TSVs through the bridge for vertical electrical and power paths.

4. What is an EMIB substrate?

An EMIB substrate is a package substrate containing embedded silicon bridges beneath selected die interfaces. The bridges handle fine-pitch routing, while the surrounding substrate carries broader signals, power, and ground.

5. What is the difference between EMIB and CoWoS?

EMIB places localized silicon bridges directly inside the package substrate. CoWoS is an interposer-based packaging family, while CoWoS-L combines localized silicon interconnects with a broader RDL interposer structure.

6. What is the difference between EMIB and EMIB-T?

Standard EMIB mainly provides lateral die-to-die routing through an embedded silicon bridge. EMIB-T adds TSVs through that bridge, creating vertical electrical paths that can support more demanding power-delivery requirements.

You may also like

EMIB-T Substrate Explained: Structure, TSV Power Delivery and Manufacturing Challenges

October 1st, 2026

An EMIB-T substrate is a package substrate containing embedded silicon bridges with through-silicon vias (TSVs). The bridges provide dense connections between adjacent chips; their TSVs add a vertical power-delivery route through the silicon. This architecture supports high-bandwidth memory (HBM) and multi-chip computing packages without requiring a full-area silicon interposer. It is a semiconductor packaging structure, not a conventional system PCB. Its manufacturing challenge is integrating small silicon bridges into a much larger substrate while maintaining alignment, electrical continuity and mechanical reliability.

Conceptual EMIB-T package with logic die, HBM, embedded silicon bridge and bridge TSVs

Key Takeaways

  • An EMIB-T substrate uses localized silicon bridges embedded inside the package substrate rather than placing the entire multi-die system over one large silicon interposer.
  • The defining development from conventional EMIB to EMIB-T is the addition of through-silicon vias (TSVs) in the bridge, enabling vertical connections and more direct power delivery.
  • EMIB-T combines fine-pitch lateral die-to-die routing with vertical electrical paths, which is increasingly important for high-power AI accelerators and HBM-based packages.
  • Intel has positioned EMIB-T for large AI and HPC packages involving HBM4/HBM4e, UCIe chiplet links, and packages extending well beyond a single reticle.
  • EMIB-T and CoWoS-L both use localized silicon for high-density connections, but their package architectures, interposer structures, routing approaches, and assembly flows differ.
  • As package dimensions and power rise, warpage, thermal behavior, power integrity, bridge alignment, TSV reliability, and known-good-die management become increasingly important.

What Is an EMIB-T Substrate?

An EMIB-T substrate integrates TSV-equipped silicon bridges into a semiconductor package substrate. EMIB means Embedded Multi-die Interconnect Bridge; EMIB-T is the TSV-enabled evolution of that technology.

Intel EMIB packaging concentrates fine interconnects where neighboring chip edges need them. The surrounding substrate carries broader package routing and mechanical support. This avoids treating every connection as though it needs the same fine-pitch silicon routing.

At EBest Circuit, our work is downstream of this packaging stage. We support system-level boards and PCB assembly, not fabrication of the embedded bridges or EMIB-T substrates.

How Does EMIB-T Work?

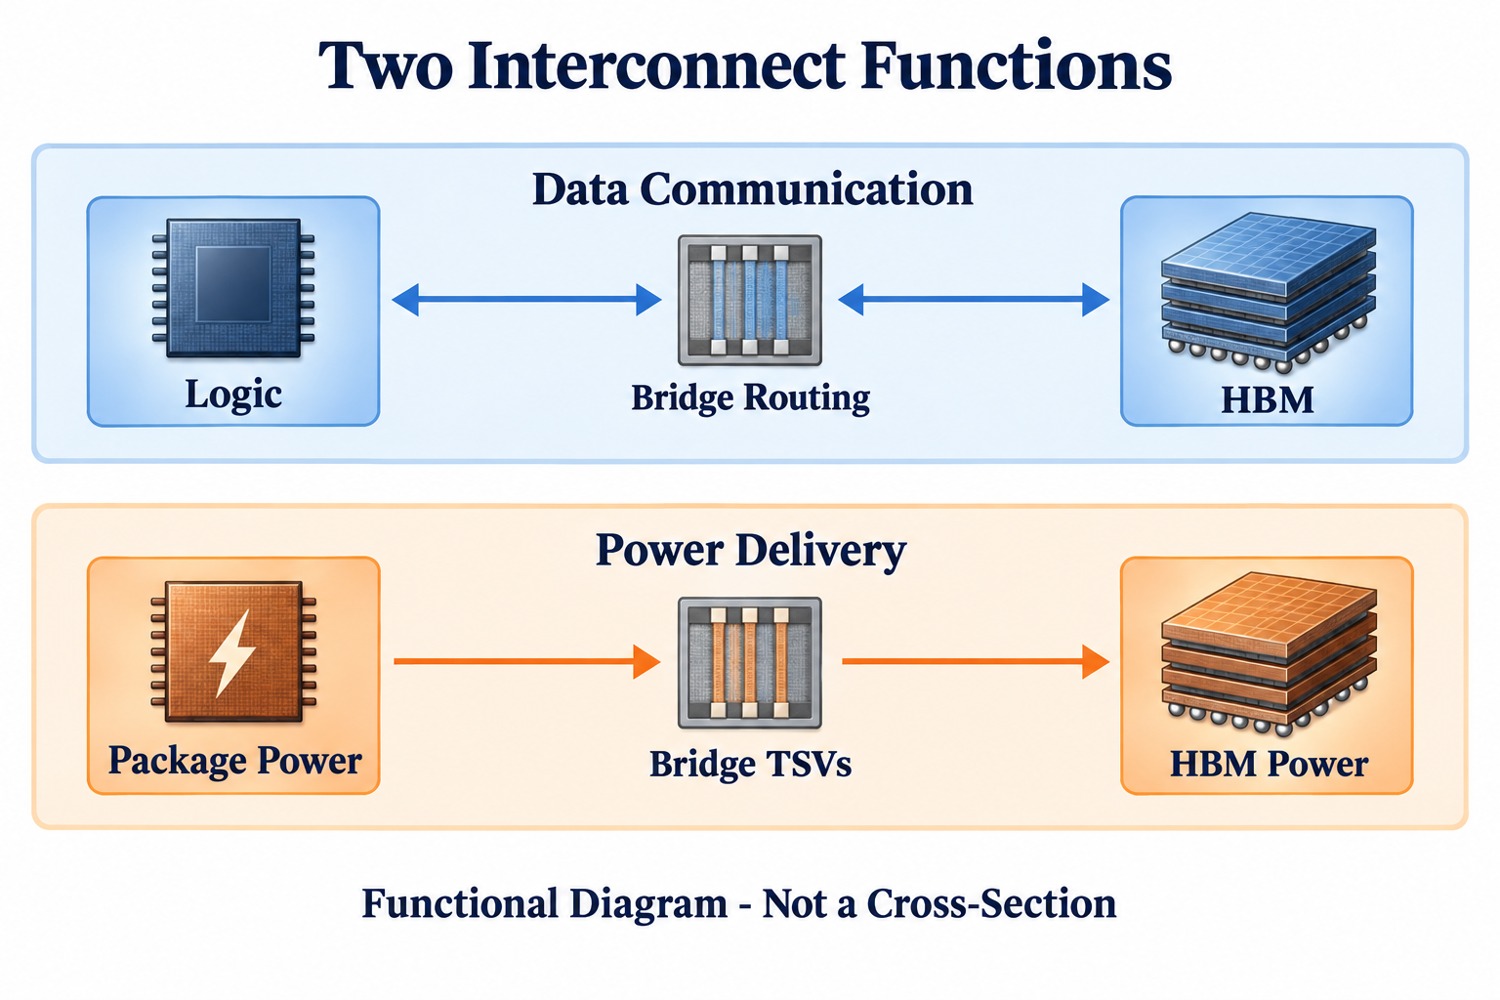
EMIB-T combines short chip-to-chip signal paths with a power route that passes vertically through the bridge. The two functions share an integration region but are not interchangeable electrical nets.

  • Data: one die connects through fine-pitch joints to bridge wiring, which reaches the neighboring die.
  • Power: package conductors connect through bridge TSVs toward the die power connections.
  • System interface: the rest of the package routing connects the assembled device to its external terminals.

The functional diagram separates these paths. It does not represent a production cross-section or a specific pin assignment.

Functional diagram separating logic-to-HBM data communication from power delivery through bridge TSVs

What Is Inside an EMIB-T Package Substrate?

The substrate combines organic dielectric and copper routing with embedded silicon bridges and their vertical connections. The logic dies and HBM sit above this structure; external package connections sit below it.

Element Function
Organic substrate structure Mechanical support and package-level routing
ABF build-up dielectric and copper Insulation between conductive routing layers in ABF-based implementations
Embedded silicon bridge Localized high-density interconnect between chip edges
Bridge TSVs Electrical connections through the silicon thickness
Fine-pitch bumps Connections between die pads and bridge-side routing
Bonding and dielectric materials Attachment, insulation and mechanical integration
External BGA connections, where specified Connection from the completed package to the system PCB

Ajinomoto Build-up Film provides electrical insulation for high-performance package substrates. It should not be confused with the glass-reinforced core that a particular substrate may also contain. Our ABF substrate materials and supply guide explains the wider material and sourcing context. An actual stackup still requires the package supplier’s approved material set.

EMIB vs EMIB-T: Key Differences

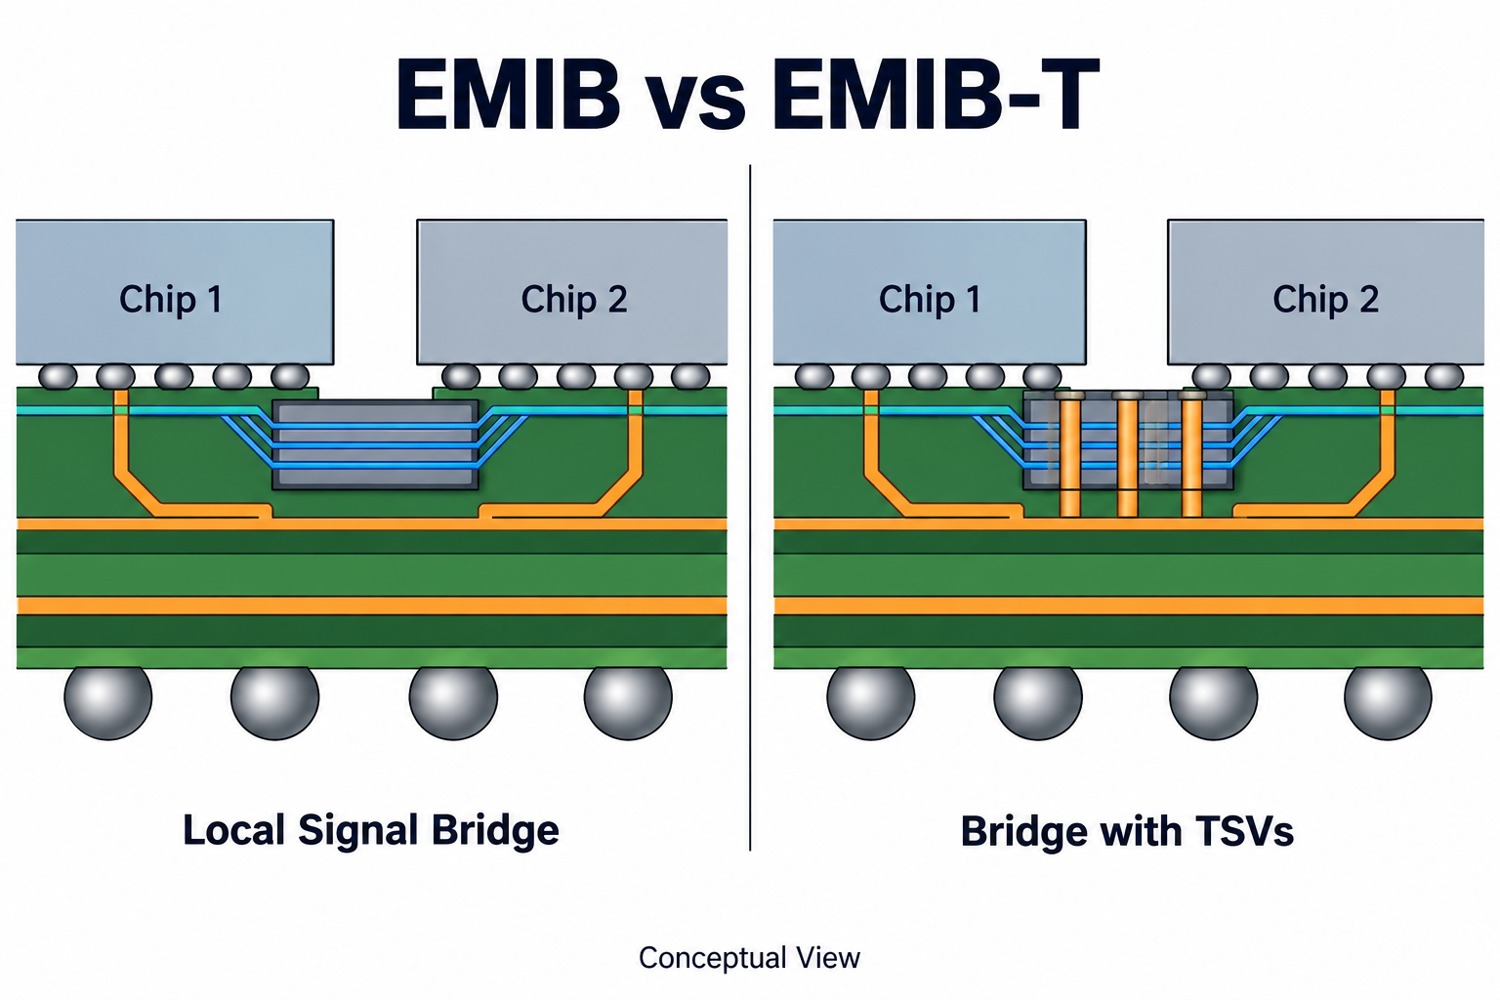
The defining difference is that EMIB-T adds through-silicon connections to the embedded bridge. Conventional EMIB already provides lateral die-to-die interconnects; it does not need bridge TSVs to perform that role.

Feature Conventional EMIB EMIB-T
Local silicon bridge Yes Yes
Bridge TSVs Not part of the basic architecture Added to enable vertical connections
Bridge-region power access Supplied through surrounding package routing Additional direct path through the bridge
Integration requirements Bridge placement and fine-pitch die connections Those requirements plus TSV and backside connection integration
Conceptual comparison of a local EMIB signal bridge and an EMIB-T bridge with TSVs

Why Does EMIB-T Add TSVs to the Silicon Bridge?

TSVs provide a more direct power route through a region that would otherwise require routing around the bridge. Intel identifies vertical power delivery with low DC and AC noise as a driver for EMIB-T, particularly for HBM.

Intel’s AI and HPC platform brief also describes bridge-integrated MIM capacitors and reduced-impedance vertical power delivery. TSVs provide a conductive path; capacitors provide local charge storage. Neither removes the need to analyze the complete power-distribution network.

Resistance contributes to DC voltage drop, while inductance affects transient voltage when current changes. Short bridge signal routes still require suitable bump geometry, reference paths and decoupling. Electrical benefit therefore depends on the complete package design, not TSV presence alone.

What Is the EMIB-T Process Flow?

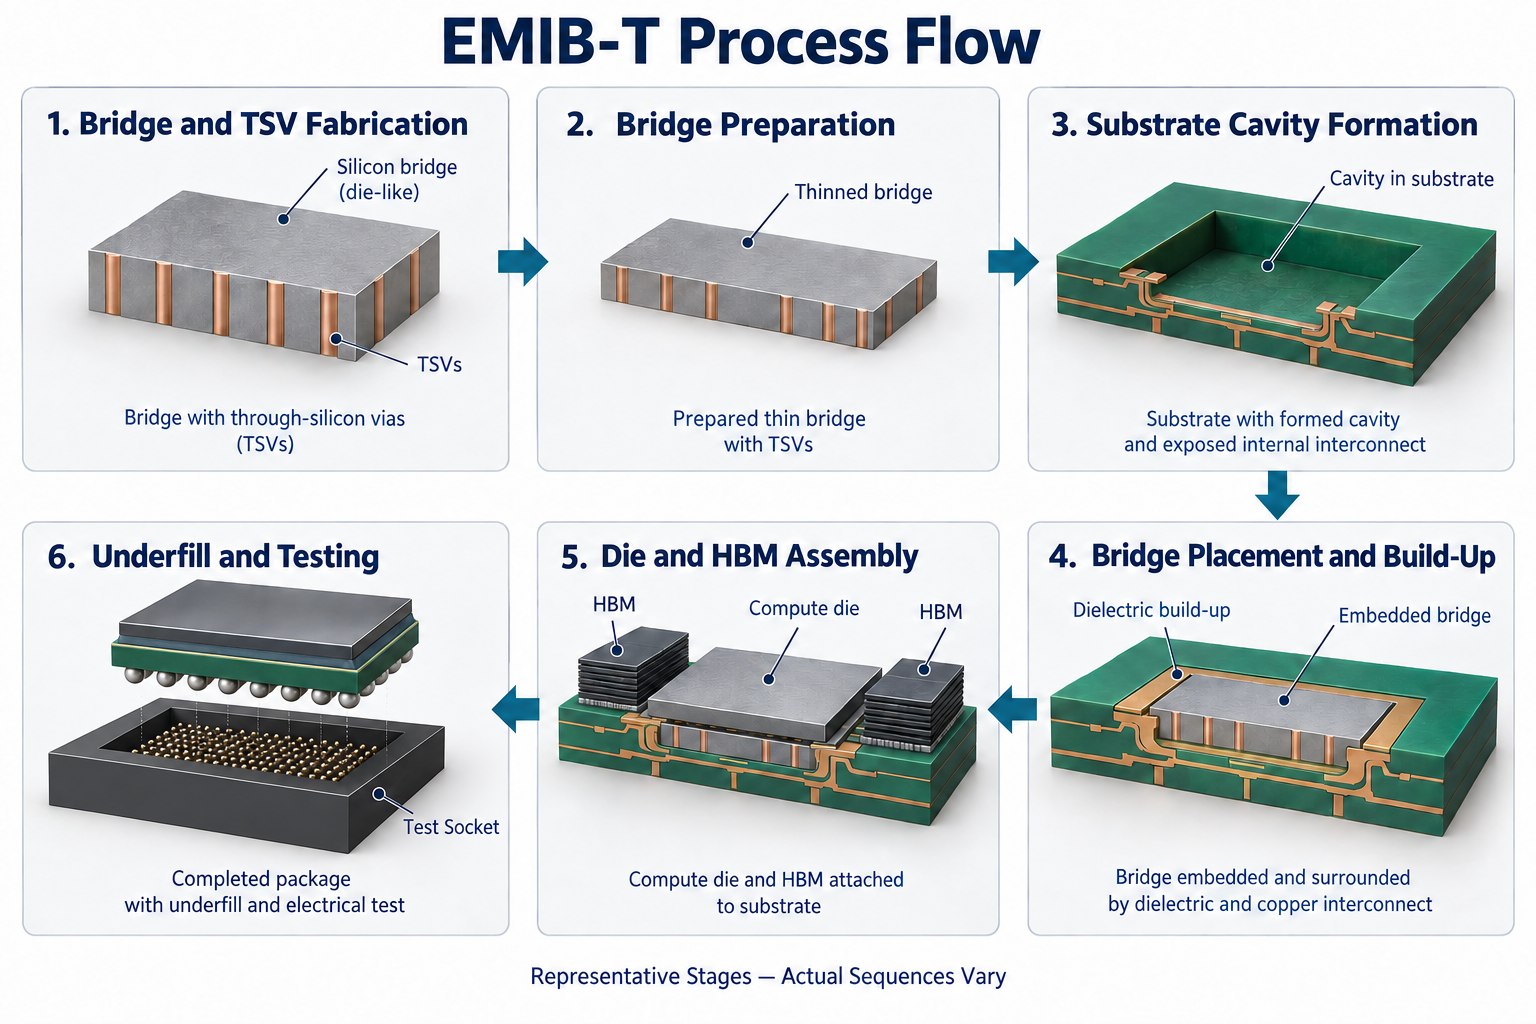
The EMIB-T process flow combines TSV-equipped bridge preparation, embedding, substrate build-up and multi-die assembly. The stages below summarize integration tasks, rather than a fixed Intel manufacturing recipe.

  1. Prepare the silicon bridge: form fine routing and TSV connections, then prepare the bridge for integration. TSV formation, thinning and backside processing follow the selected bridge process.
  2. Prepare substrate cavities: create the local spaces and underlying connection structures required by the package layout.
  3. Place and bond the bridges: control lateral registration, seating height and attachment quality.
  4. Build dielectric and copper layers: integrate the bridge with surrounding substrate routing and connection pads.
  5. Assemble logic dies and HBM: connect the die interfaces to the bridge and package substrate using the specified assembly flow.
  6. Reinforce and test: complete applicable underfill or bonding operations, electrical checks and reliability qualification.

Intel’s EMIB product brief describes cavity embedding, attachment and dielectric/metal build-up. EMIB-T adds vertical bridge integration; exact TSV processing order and acceptance limits depend on the qualified implementation.

Six representative EMIB-T integration stages from bridge fabrication to testing

Why Is EMIB-T Substrate Manufacturing Difficult?

Manufacturing must align a small, rigid silicon insert with multilayer substrate wiring and die contacts through repeated processing steps. The EMIB process flow already requires this registration; EMIB-T adds the bridge’s vertical connections. Placement accuracy at one temperature does not prove alignment after bonding or subsequent thermal cycles.

  • Lateral registration: bridge pads must align with the next interconnect level.
  • Height control: bridge and substrate surfaces must support consistent connections rather than uneven contact.
  • Thermomechanical compatibility: different expansion behavior can produce local stress and displacement.
  • Bonding integrity: attachment materials must bond without defects that undermine the structure.
  • TSV reliability: evaluate copper continuity and interface stress through the specified thermal-cycling and electrical tests.
  • Thermal design: co-design the die layout, thermal interface material and cooling hardware to manage local heat concentration.
  • Known-good dies: screen expensive die inputs and use staged electrical checks to limit the cost of late assembly failures.

What Causes EMIB-T Yield Challenges?

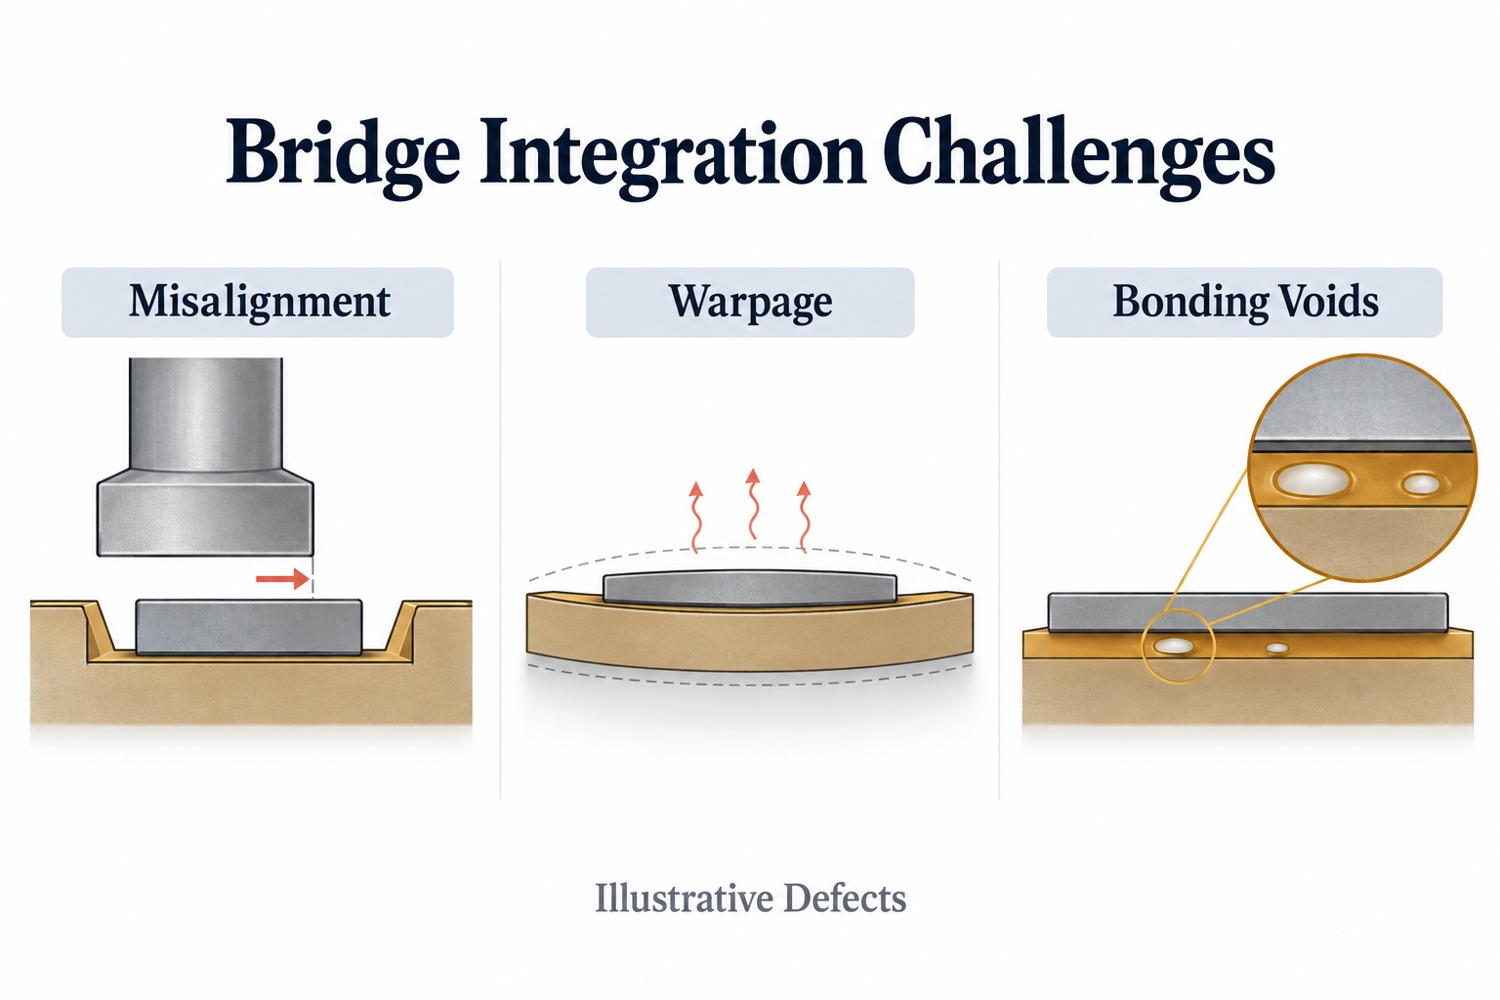
Misregistration, nonuniform height and bonding defects can make otherwise usable bridge and substrate components fail after integration. More interfaces also create more opportunities for a defect to interrupt an electrical path.

A September 23, 2026 TrendForce News report, citing supply-chain sources, put EMIB substrate yield at approximately 45%. Its reported targets were 50% in Q4 2026 and 60% in Q1 2027. These are reported substrate-stage figures and future targets, not Intel-published production data or a verified yield for every EMIB-T package.

The September 2026 supply-chain report specifically discussed thermal-expansion mismatch, bridge positioning and bubbles in non-conductive film beneath bridge TSV connections. Those are reported production challenges, not a published defect breakdown across all suppliers.

A useful yield discussion must identify the tested population. Bridge-wafer yield, integrated-substrate yield and final electrical package yield have different denominators. A quoted percentage without its process stage, product complexity and test criteria cannot reliably predict delivered device availability.

Illustrative bridge integration defects showing misalignment, warpage and bonding voids

EMIB vs CoWoS: What are Differences?

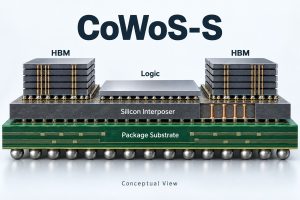
EMIB embeds local silicon bridges in the package substrate; TSMC describes CoWoS as a family of interposer-based technologies. CoWoS-S uses a continuous silicon interposer, whereas CoWoS-L combines an RDL interposer with local silicon interconnects.

Architecture High-density interconnect structure
EMIB-T Local TSV-equipped silicon bridges embedded in the package substrate
CoWoS-S Silicon interposer spanning the integrated die arrangement
CoWoS-L RDL-based interposer incorporating local silicon interconnects

Local bridges reduce the silicon area devoted to interconnection, but add integration demands at each bridge location. A larger silicon interposer supports routing across a wider area; its manufacturing approach is different. Neither description proves that one complete package is always cheaper or has better yield.

For a closer structural comparison, our CoWoS-L explanation distinguishes local silicon interconnects from the surrounding RDL. CoWoS-L is not an all-silicon interposer, and it is not simply another name for EMIB-T.

How Does EMIB-T Support HBM4, HBM4e and UCIe?

EMIB-T supports dense memory and chiplet interfaces by combining short lateral silicon routes with vertical power access through the bridge. AI accelerators and HPC processors need both: more data connections alone do not solve the power demands of the connected dies.

  • HBM4/HBM4e: wide logic-to-memory interfaces need dense routing close to the compute die. Bridge TSVs add power paths through that crowded region.
  • UCIe: short chiplet links need controlled interconnect geometry and return paths, alongside the power network.
  • Large packages: placement and routing must be evaluated together with thermal and mechanical behavior.

In its ECTC 2026 technology update, Intel reported these development results:

  • 25 μm first-level interconnect bump pitch.
  • 120 × 120 mm package dimensions.
  • More than nine reticle areas of compute and memory silicon in one package.
  • Signal and power co-optimization supporting 12 Gb/s HBM4e and 64 Gb/s UCIe transmission.

These are technology-development results, not universal specifications for every production package. Separately, Synopsys’ EMIB-T design-flow discussion describes large-design demands including footprints of 120 × 180 mm. That design context should not be combined with Intel’s demonstration dimensions into a single qualified manufacturing range.

Where Is EMIB-T Used in AI and HPC Packaging?

EMIB-T is designed mainly for large AI and HPC packages that integrate multiple compute dies, HBM stacks, and high-speed chiplet interfaces.

Typical applications include:

  • AI training accelerators;
  • AI inference processors;
  • HPC accelerators;
  • multi-die GPU or XPU packages;
  • chiplet-based CPUs;
  • UCIe-based heterogeneous processors;
  • multi-HBM compute modules;
  • data-center processors.

The package has to move large volumes of data between dies, feed high current to compute silicon, connect several HBM stacks, and control thermal and mechanical stress at the same time.

EMIB-T is particularly relevant where localized high-density silicon routing is needed but using one continuous silicon interposer across the whole package is not the preferred architecture.

Is an EMIB-T Substrate the Same as a PCB?

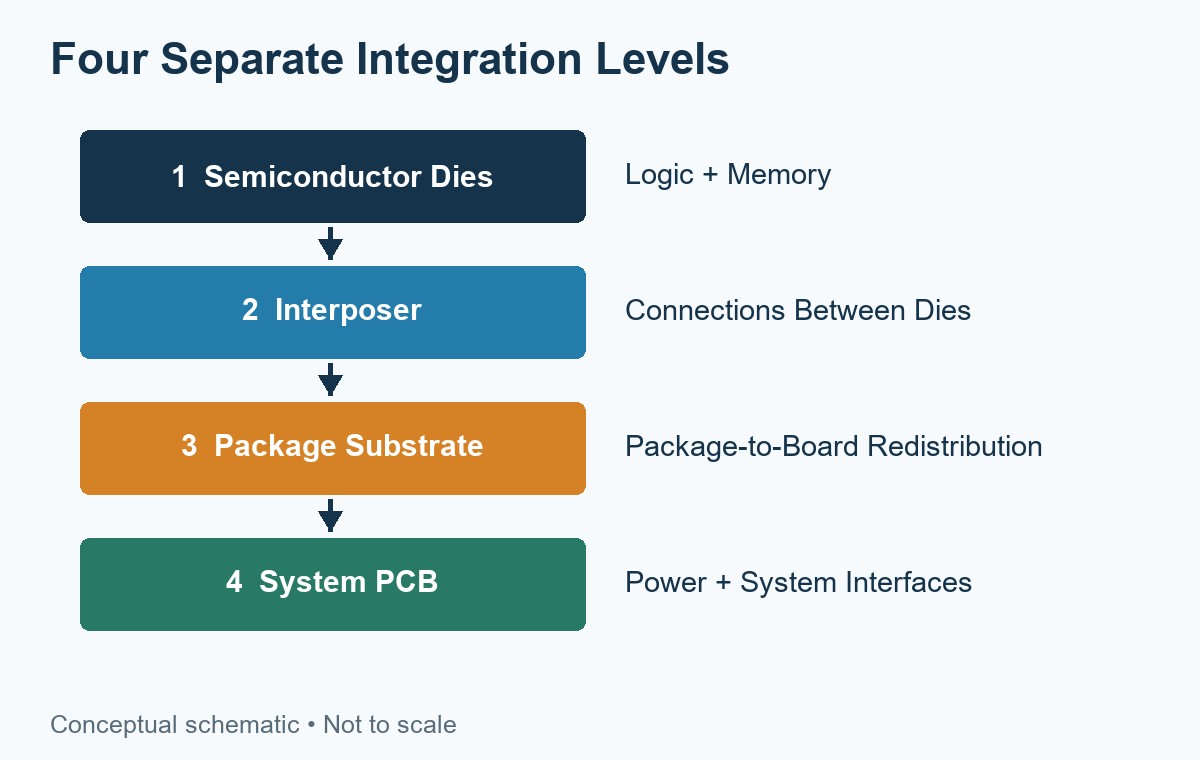
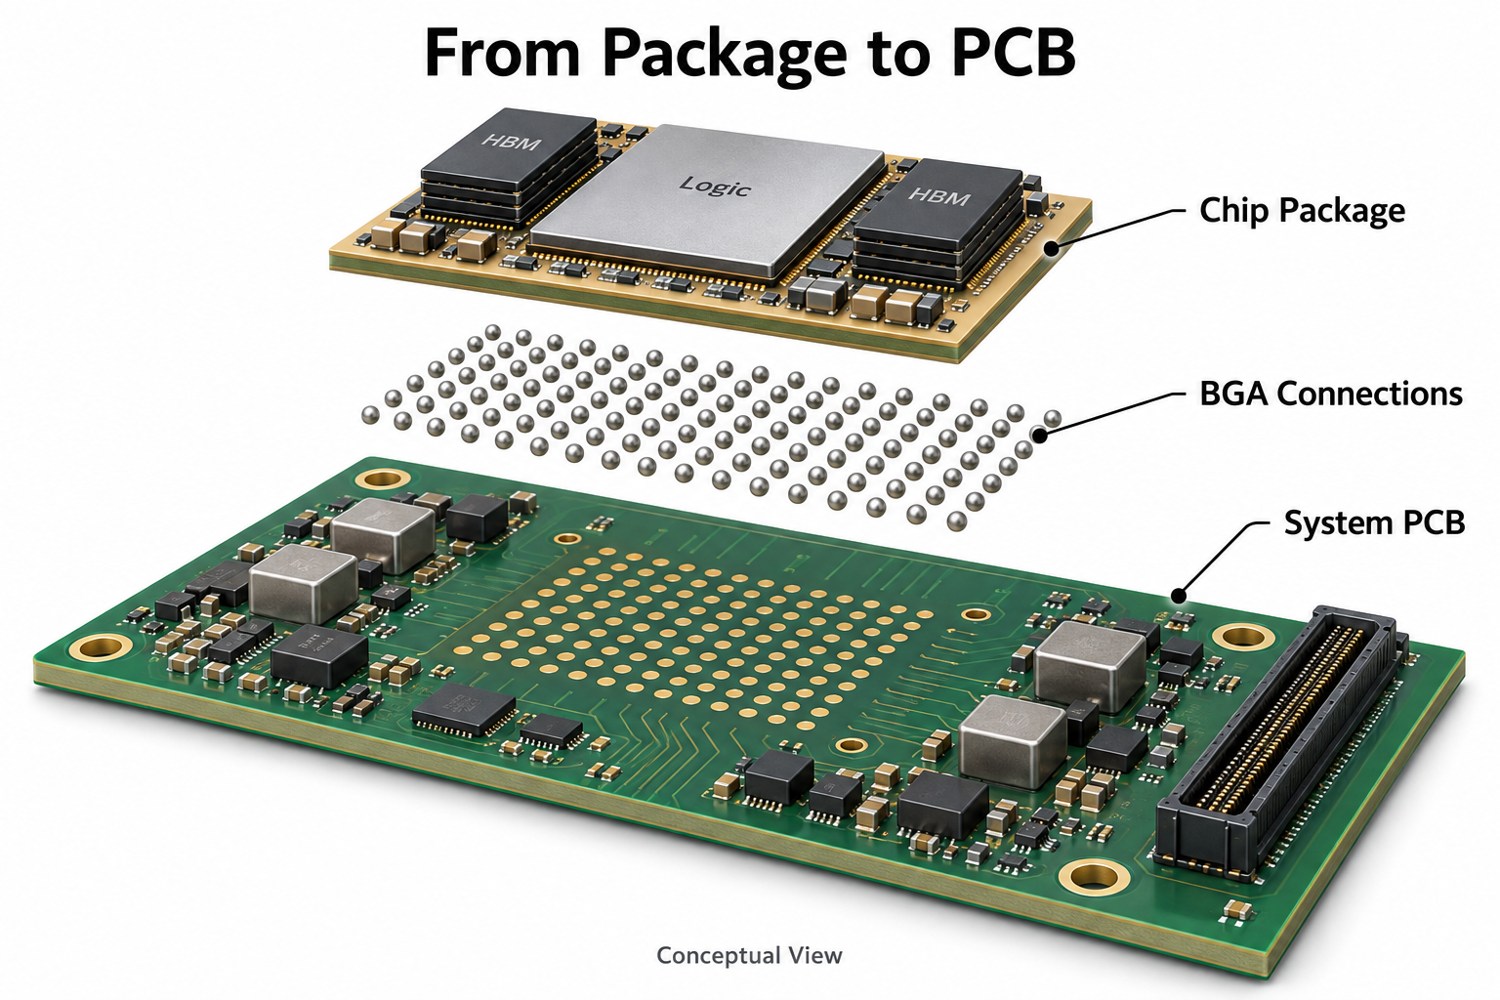
No. The EMIB-T substrate is part of the semiconductor package; the system PCB connects that completed package to the rest of the electronic system.

A TSV passes through silicon. A package-substrate microvia passes through a dielectric layer. A PCB via connects copper layers in a board. They differ in materials, dimensions and manufacturing processes, even though all provide electrical connections between levels.

For a BGA-mounted device, the board land pattern comes from the external ball map and package drawing—not from the pitch of the bridge’s internal microbumps. Using an internal packaging dimension as a PCB footprint dimension would address the wrong interface.

Exploded conceptual view separating the chip package, external BGA connections and larger system PCB

FAQ About EMIB-T Substrates

Is EMIB-T the same as EMIB-M?

No. Intel’s technology brief uses EMIB-M for bridge-integrated metal-insulator-metal capacitors and EMIB-T for the TSV-enabled solution. Later descriptions of EMIB-T also discuss MIM capacitors. TSVs and capacitors perform different functions, so the names should not be treated as interchangeable material grades.

Does EMIB-T require a glass-core substrate?

No. Public Intel descriptions include organic-substrate implementations. EMIB-T identifies the embedded-bridge technology, not a universal core material. A proposed glass-core implementation would require its own approved stackup and reliability evidence; it should not be assumed from the EMIB-T name.

Is EMIB-T the same as Foveros?

No. EMIB-T provides local bridge connections between neighboring dies, while Foveros technologies support other integration arrangements, including vertical die stacking. Intel describes combining the technologies in EMIB 3.5D. A combined package does not make their interconnect structures identical.

Can an existing package move to EMIB-T without redesign?

Not automatically. Die interfaces, bump assignments, power paths and mechanical constraints need to match the chosen packaging flow. Synopsys’ reference-flow announcement includes early bump and TSV planning and multiphysics analysis, illustrating why a technology migration is an engineering project rather than a material substitution.

Can PCB-level X-ray inspection certify the internal silicon bridge?

No. Inspecting board-level solder joints does not qualify buried package interconnects. Package acceptance requires the package supplier’s electrical and reliability evidence. PCB assembly inspection evaluates the board-level work and cannot replace semiconductor-package qualification.

What Does EMIB-T Mean for PCB and PCBA Projects?

For downstream manufacturing, the practical requirement is a released package specification and a board design matched to it. The packaging architecture alone does not set PCB layer count, laminate grade or assembly temperature.

  • Footprint and routing: confirm the package drawing, ball map and approved land pattern before PCB design review.
  • Power and thermal requirements: use device-level current and cooling specifications to review the board power network and mechanical clearances.
  • Assembly plan: check the supplied component’s handling, moisture sensitivity and mounting instructions, together with the agreed inspection and functional-test scope.

At EBest Circuit, we support PCB fabrication, component sourcing and PCBA projects, with suitability confirmed against the actual design. Send the processor package specification, PCB files, BOM, quantities and test requirements to sales@bestpcbs.com for a project-specific review.

You may also like

Types of Motors: Differences, Uses and Drive Selection

September 25th, 2026

The main types of motors used in electrical equipment include brushed DC, brushless DC (BLDC), AC induction, synchronous, stepper and universal motors. Servo motors are also common, but “servo” describes a feedback-controlled motion system rather than one electromagnetic construction. Choosing between them starts with the required torque, speed, positioning accuracy and power supply—not simply whether a product runs from a battery or the mains.

This guide focuses on electric motors and the electronics that drive them. Hydraulic and pneumatic motors use different energy sources and fall outside this comparison.

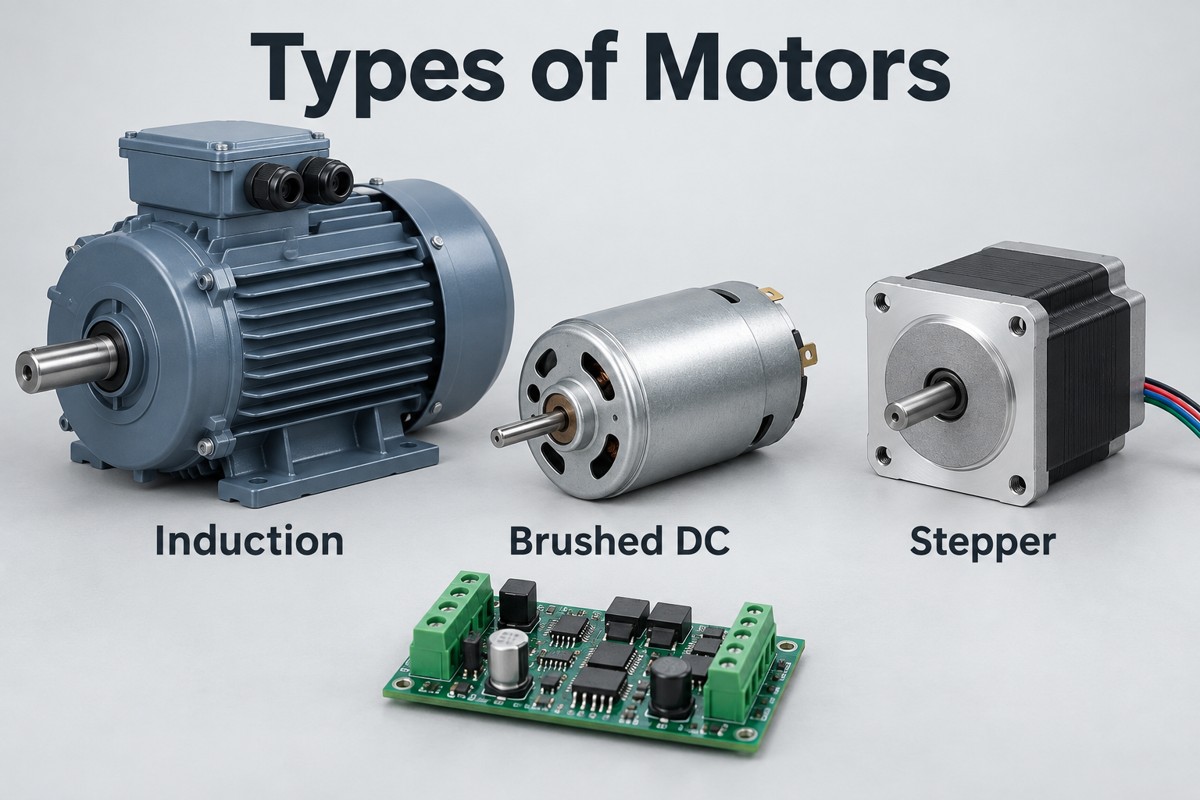
Induction, brushed DC and stepper motors with a motor driver PCB

Key Takeaways

  • Electric motors convert electrical energy into motion; their construction, supply and control method are separate ways to classify them.
  • Brushed DC motors use mechanical commutation. BLDC motors need electronic commutation and a compatible driver.
  • Induction motors develop torque with slip; synchronous motors follow the rotating magnetic field at synchronous speed in steady operation.
  • Servo is a control-system description, not an alternative to every AC or DC motor category.
  • Steppers offer incremental positioning, but microstepping resolution does not guarantee equal positioning accuracy.
  • Selection requires the torque–speed curve, acceleration, duty cycle and thermal conditions—not rated power alone.
  • Motor driver PCB design must account for current paths, switching loops, heat, sensing and protection; assembly inspection does not replace loaded functional testing.

What Are the Main Types of Electric Motors?

The main electric motor types are brushed DC, BLDC, induction, synchronous, stepper and universal motors. Servo systems add feedback-controlled motion and can use several motor constructions, so they are listed separately below.

Motor or system Operating principle Typical applications
Brushed DC Brushes and a commutator switch rotor current Small actuators, simple pumps, low-cost drives
BLDC Electronic switching energizes stator windings around a permanent-magnet rotor Fans, battery tools, compact pumps
AC induction A rotating stator field induces rotor current Conveyors, industrial pumps, ventilation
Synchronous Rotor rotation stays synchronized with the stator field Controlled industrial drives, traction, compressors
Stepper Sequenced winding currents produce incremental rotation Printers, dosing mechanisms, positioning stages
Universal A series-wound commutator design operates on suitable AC or DC Some corded tools and household appliances
Servo system Feedback corrects motion against a command Robot joints, CNC axes, packaging machines

A gearmotor adds a gearbox to a motor; it is not a separate electromagnetic principle. Likewise, “linear” describes motion along a line rather than rotation. An AC synchronous motor can therefore also be part of a geared servo axis.

At EBest Circuit, we support the electronics behind these systems through PCB fabrication, component sourcing and PCB assembly services. For a motor controller, the manufacturing review starts with its power stage, board construction and assembly requirements—not with a claim that one PCB suits every motor.

How Do AC and DC Motor Classifications Differ?

AC and DC usually describe the electrical supply or the way a motor is driven, but modern electronic drives make that distinction less straightforward. A battery supplies DC, while an inverter can convert it into alternating phase currents for a synchronous motor.

Induction and synchronous machines are familiar AC categories. Brushed motors can connect to a suitable DC source, whereas BLDC motors require a commutating controller. Check the motor terminals, drive documentation and winding ratings rather than classifying a motor from the equipment’s input plug alone.

How Do Brushed DC and BLDC Motors Differ?

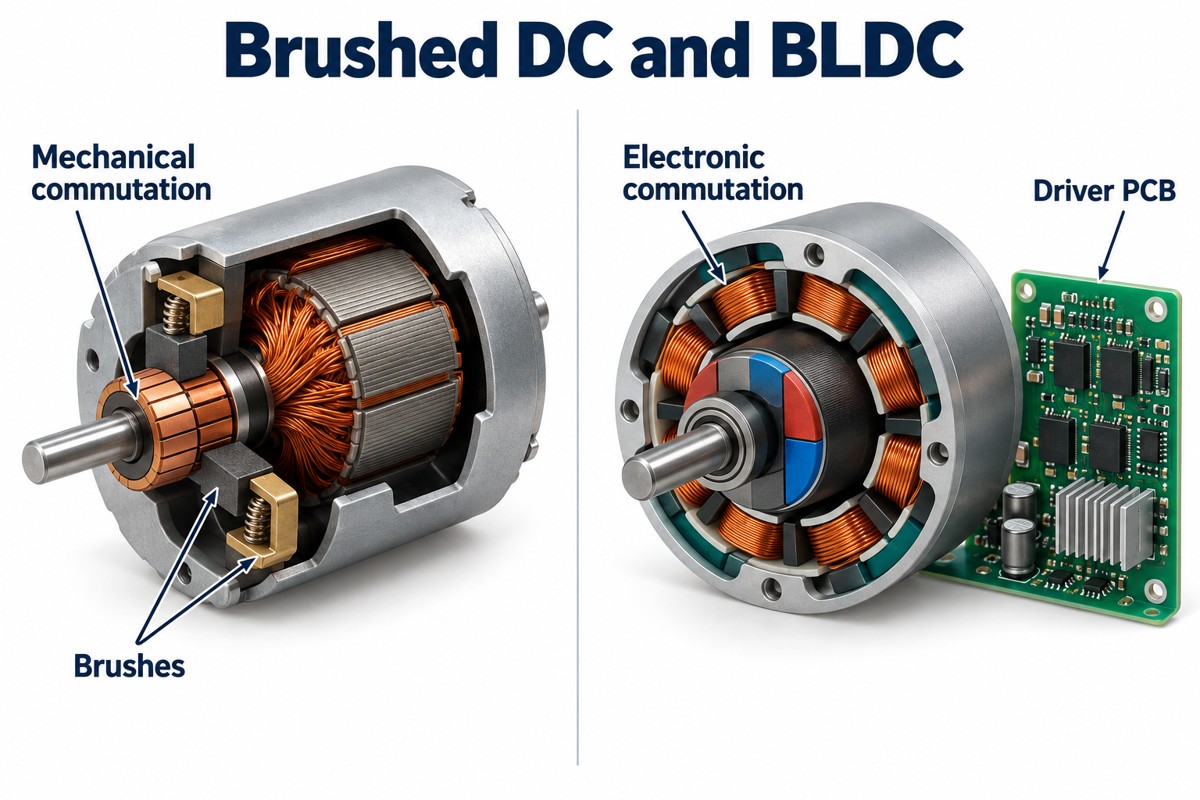
Brushed DC motors switch current mechanically; BLDC motors switch it electronically. Brushes simplify the external drive but introduce contact wear and electrical noise, while BLDC designs move the switching task into the controller.

Mechanical brush commutation compared with electronic BLDC commutation
  • Brushed DC: a single switching stage can provide one-direction speed control; an H-bridge supports reversal and controlled braking.
  • BLDC: a typical three-phase drive uses three half-bridges. Rotor position can come from sensors or estimation, depending on the controller.
  • Maintenance: eliminating brushes removes brush wear, but bearings, insulation and electronics still have operating limits.

BLDC and permanent-magnet synchronous motor (PMSM) terminology overlaps. BLDC commonly refers to trapezoidal back-EMF and block commutation, while PMSM often refers to sinusoidal operation. The actual motor and control algorithm matter more than the label on a product listing.

What Is the Difference Between Induction and Synchronous Motors?

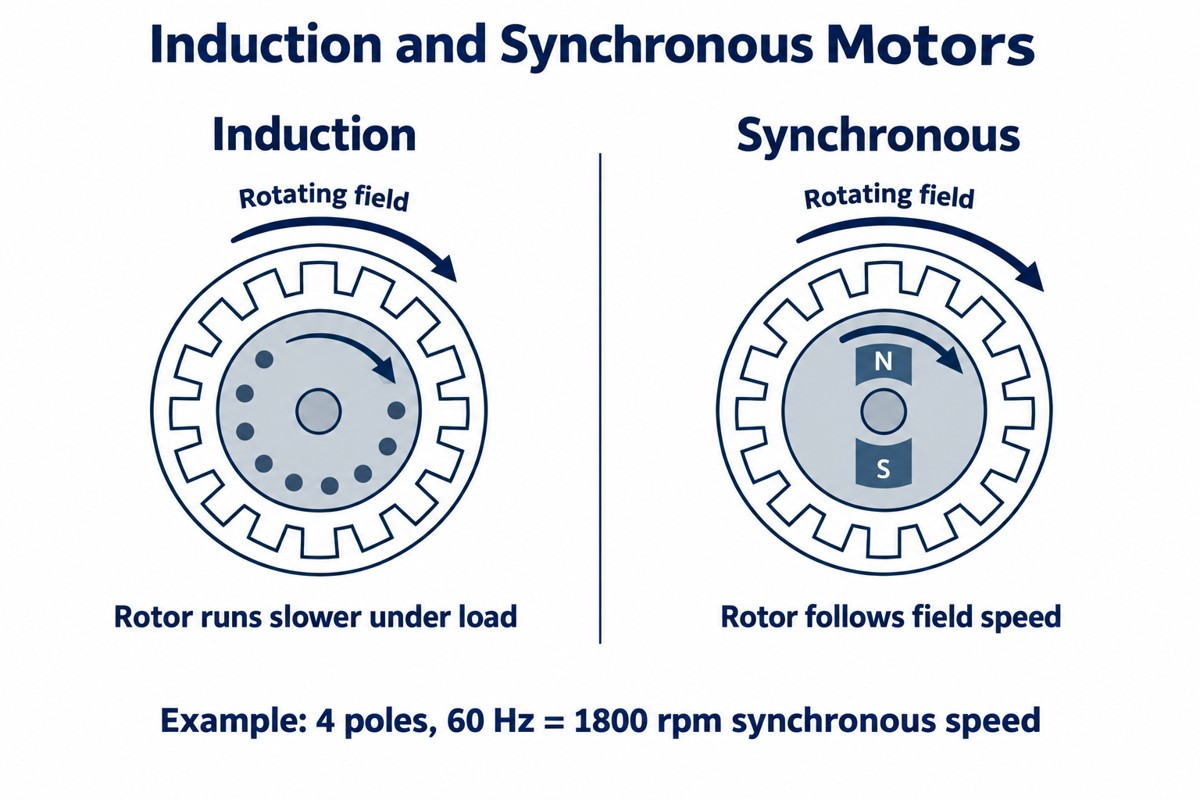
An induction motor’s rotor normally runs below the rotating field speed when producing motoring torque; a synchronous motor’s rotor follows that field speed in steady operation. The speed difference in an induction machine is called slip.

Synchronous speed is n = 120f/P, where n is rpm, f is electrical frequency in hertz and P is the number of poles. A four-pole motor at 60 Hz has a synchronous speed of 1,800 rpm. If an induction motor runs at 1,750 rpm under the stated load, its slip is approximately 2.8%; that is an illustrative operating point, not a universal rating.

Induction rotor slip compared with synchronized rotor and field speeds

Induction motors are practical for continuous industrial rotation. Permanent-magnet synchronous drives can offer efficient, compact controlled motion, but need a suitable starting and control arrangement. A variable-frequency drive changes electrical frequency; neither category is inherently limited to one shaft speed.

When Should You Choose a Stepper or Servo System?

Choose a stepper for incremental positioning within a known torque–speed envelope; choose a servo system when feedback-based error correction and dynamic response justify the additional control hardware. Load changes, acceleration and required settling time determine the better fit.

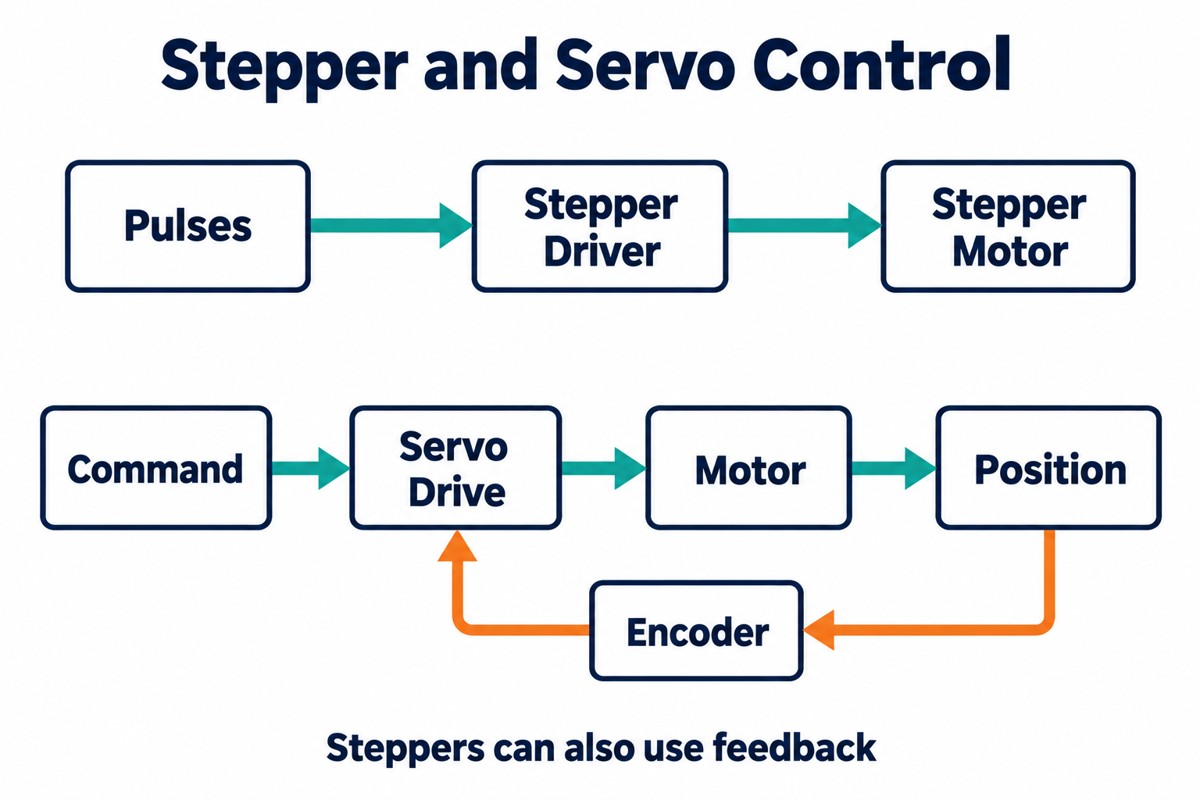
A common 1.8° stepper makes 200 full steps per revolution. With 16 microsteps per full step, the driver receives 3,200 step commands per revolution, but that does not establish 3,200 equally accurate mechanical positions. Friction, load torque and motor construction affect the result.

Open-loop stepper command path and encoder feedback loop in a servo system

An open-loop stepper can lose position if the commanded motion exceeds available torque. A servo measures motion and adjusts its output, although it still needs tuning and suitable mechanical sizing. Closed-loop stepper products also exist, so “stepper means no feedback” is not a reliable rule.

Which Types of Motors Are Used in Common Applications?

Fans and pumps usually need sustained rotation, while robots and positioning equipment need controlled motion. Those different loads explain why equipment in the same industry may use several motor technologies.

  • Types of motors used in robotics: geared brushed DC motors can drive simple mobile platforms; BLDC/PMSM servo systems suit controlled joints; steppers suit indexing and smaller positioning mechanisms.
  • Types of motors in HVAC: induction motors appear in fans and pumps, while electronically commutated permanent-magnet motors support variable-speed blowers. Compressor motor selection depends on the compressor and drive architecture.
  • Types of motors in cars: brushed and brushless motors serve auxiliary actuators, fans and pumps. Electric traction can use permanent-magnet synchronous or induction machines, among other architectures.

A motor suitable for a small robot wheel is not automatically suitable for a vertical lifting axis. Holding requirements, a mechanical brake and the consequences of losing power must be considered separately from normal running torque.

How Do You Select the Right Motor for a Load?

Select a motor whose continuous and peak torque cover the required speed, acceleration and duty cycle without exceeding its thermal limits. Rated wattage alone cannot show whether it will start the load or survive repeated stops.

  1. Define motion: required shaft speed, travel, acceleration and positioning accuracy.
  2. Calculate load torque: include friction, gravity, inertia and gearbox losses where applicable.
  3. Check the torque–speed curve: confirm both the continuous operating point and short-duration peaks.
  4. Match the drive: verify supply voltage, phase current, feedback interface and braking requirements.
  5. Check temperature and duty: use the manufacturer’s specified cooling and ambient conditions.

For a calculated example, a shaft delivering 2 N·m at 1,500 rpm produces about 314 W of mechanical power, using P = T × 2πn/60. Electrical input must be higher because the motor and drive have losses. Starting torque can still exceed this steady operating requirement.

How Does Motor Type Affect the Driver PCB?

Motor type determines the power-stage arrangement, current regulation and feedback interfaces on the driver PCB. A reversible brushed motor typically needs one H-bridge; a bipolar two-phase stepper needs two; a typical three-phase BLDC drive needs three half-bridges.

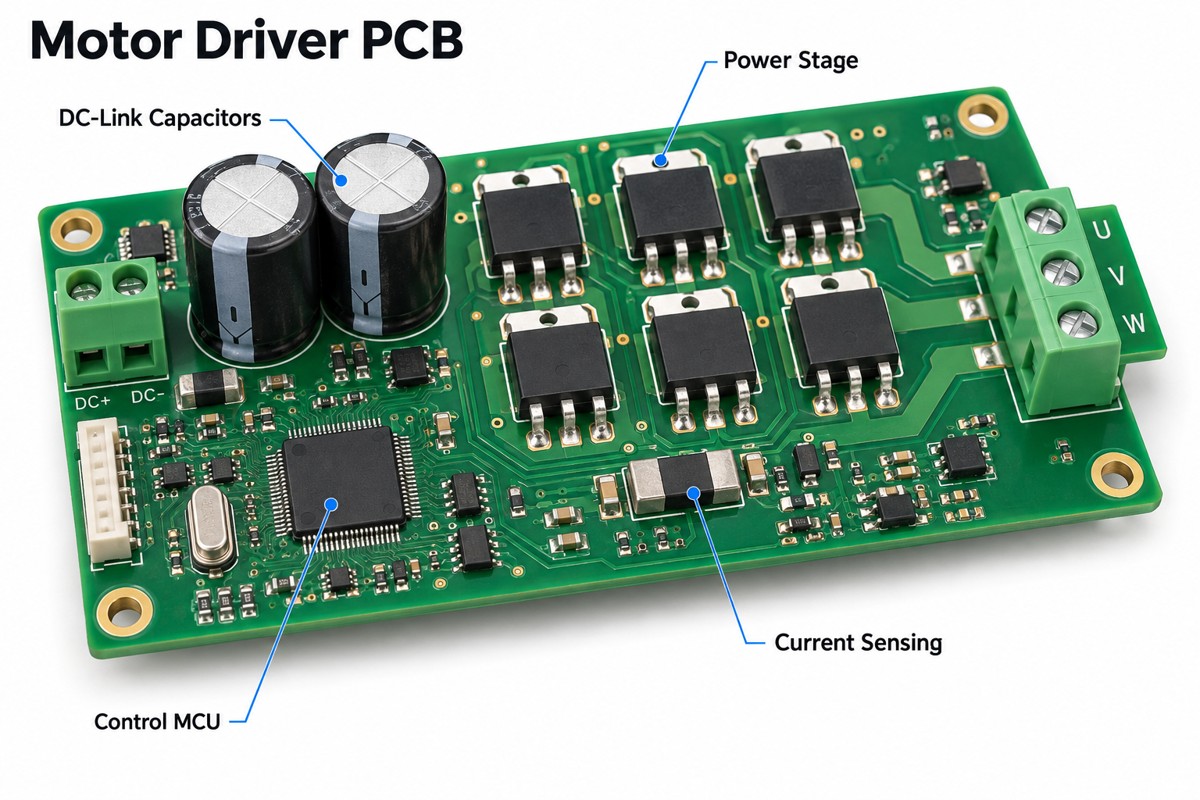
Motor driver PCB showing power stage, DC-link capacitors, current sensing and control MCU
  • Power routing: size copper paths and vias for RMS current, permissible heating and the actual stackup.
  • Switching loops: place local decoupling near the switching stage and keep high-current loops compact.
  • Sensing: route current-sense connections to avoid power-path voltage drops corrupting measurements.
  • Protection: account for overcurrent, stalled operation, reverse supply and regenerated energy as the application requires.

A heavy copper PCB can support demanding current paths, but thicker copper is not a universal fix. Trace width, layer connections, component pads and cooling still govern performance. Fine-pitch control components also need manufacturable clearances alongside the power copper.

What Should Be Checked Before a Motor Controller Enters Production?

Check assembly quality and loaded electrical behavior separately: a board can have acceptable solder joints yet fail during startup, reversal or braking. The production test plan should define operating conditions and pass/fail limits before the build.

  • Assembly: inspect power-device orientation, exposed-pad soldering, shunts and high-current connectors. Use X-ray where hidden joints require it.
  • Startup: verify current limits and successful starting with the specified load and supply range.
  • Thermal operation: measure power-stage and connection temperatures at the required duty cycle.
  • Fault response: validate the specified stall, overcurrent and sensor-fault behavior using controlled test conditions.

For PCB prototyping, provide the motor model, schematic, expected load and test procedure alongside the fabrication files. This makes it possible to distinguish a manufacturing defect from incorrect drive settings or an undersized motor.

FAQ About Types of Motors

Which types of motors for Arduino projects are easiest to start with?

A small brushed DC motor with a suitable driver, a stepper with a current-regulated module, or a hobby servo with its own control electronics are common starting points. The Arduino provides commands, not motor power. Match the separate supply and driver ratings to the motor, and follow the module’s grounding instructions.

Can every AC motor run from a variable-frequency drive?

No. The drive must match the motor type, voltage, phase arrangement and control method. Many three-phase induction motors work with appropriately selected VFDs, but single-phase capacitor motors and special-purpose motors need separate evaluation. Consult both motor and drive documentation before connecting them.

Is a higher-voltage motor always more powerful?

No. Voltage alone does not determine mechanical output. Torque, speed, current, winding design and thermal limits also matter. Two motors with the same voltage rating can have very different power ratings, while a lower-voltage system may carry more current to deliver comparable power.

Does a gearbox increase motor power?

No. A reduction gearbox trades output speed for torque and introduces losses. It can let a motor operate in a more useful speed range, but it does not create power. Check gearbox torque capacity, efficiency, backlash and permissible input speed as well as the motor rating.

Why can a motor overheat while turning slowly?

Low speed does not necessarily mean low current. A heavily loaded motor may draw substantial current while shaft-driven cooling is reduced. A stepper may also consume current while holding position. Check winding current, the duty cycle and the manufacturer’s cooling requirements rather than judging temperature from speed alone.

Need a PCB for Your Motor Control Project?

The right motor meets the load’s torque, speed and control requirements; the right driver board delivers that performance without exceeding its electrical or thermal limits. At EBest Circuit, we provide PCB fabrication, component sourcing and PCBA support for the control electronics, with inspection and functional testing agreed to the project requirements.

Send your Gerber files, BOM, quantity, motor specification and test requirements to sales@bestpcbs.com. We can review the board’s manufacturing and assembly needs and prepare a quotation for your prototype or production build.

You may also like

CoWoS-S vs CoWoS-L: Interposer and Scaling Differences

September 25th, 2026

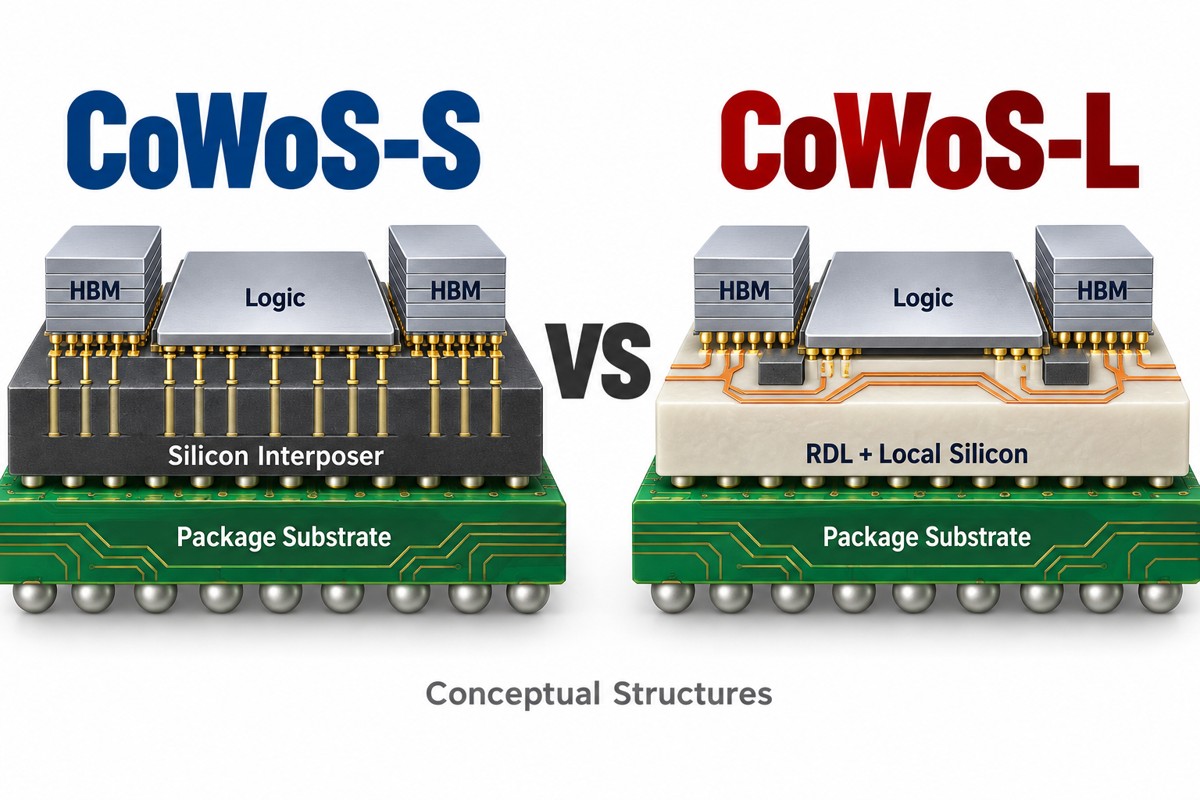
CoWoS-S vs CoWoS-L is primarily a comparison of interposer structures: S uses a continuous silicon interposer, while L combines an RDL-based interposer with embedded local silicon interconnects. Both can connect logic and HBM inside an advanced package.

L is not simply a larger version of S, and the letter does not determine a finished chip’s speed or price. The useful comparison is where dense routing is placed, how the package scales, and which design requirements each qualified implementation meets.

Conceptual comparison of a continuous CoWoS-S silicon interposer and a CoWoS-L RDL interposer with local silicon bridges

What Is the Main Difference Between CoWoS-S and CoWoS-L?

CoWoS-S places dense routing in a full silicon interposer; CoWoS-L uses local silicon bridges within a wider RDL interposer. The package substrate remains a separate structure beneath both.

Feature CoWoS-S CoWoS-L
Interposer structure Continuous silicon RDL structure with embedded LSI
Dense die-to-die routing Silicon interposer wiring Local silicon interconnect regions
Layout consideration Routing across the silicon interposer Bridge placement plus wider RDL routing
Memory integration Supports HBM configurations Supports HBM configurations
Connection to the PCB Through a separate package substrate Through a separate package substrate

This comparison describes the architecture. Exact routing rules, supported dies, dimensions, and qualification belong to the specific generation and product. TSMC’s official CoWoS technology overview is the primary reference for the structural distinction.

How Do Their Signal Paths Differ?

S routes die-to-die connections through the continuous silicon interposer; L uses local silicon regions for dense neighboring interfaces and RDL for the wider redistribution structure.

CoWoS-S schematic showing lateral routing across silicon and separate vertical connections

In an S layout, the silicon interposer is the common routing platform below the dies. In an L layout, a bridge must align with the interfaces it connects. That makes the die floorplan and local connection regions part of the architecture decision.

CoWoS-L schematic showing a local silicon bridge under adjacent die edges inside an RDL structure

Neither illustration defines all signal or power paths in a real product. A board designer should not infer package pin assignments, routing pitch, or electrical models from a simplified cutaway.

The engineering comparison is routing availability versus routing localization. S offers a continuous silicon platform on which to organize connections among the dies. L requires dense interfaces to line up with local silicon regions, while wider redistribution uses the surrounding RDL. L therefore makes bridge placement an explicit floorplanning constraint; S still has congestion, layer-count, and interposer-area constraints.

Which Architecture Supports Larger Interposer Areas?

CoWoS-L is TSMC’s local-silicon approach for extending the interposer platform beyond the area served by its published CoWoS-S offering.

The public overview lists S up to 3.3 reticles, approximately 2,700 mm², and identifies a 3.5-reticle L generation in production since 2024. These figures describe particular platform generations, not a fixed area ratio or a universal limit on every future product.

Compare dated, qualified configurations. Do not compare an S production specification with an L roadmap target and describe both as equally available. Interposer area also differs from package outline, usable die area, and system PCB dimensions.

Is CoWoS-L Faster or Cheaper Than CoWoS-S?

CoWoS-L is attractive when the design needs a larger integration area while retaining dense local links; CoWoS-S remains relevant when the die arrangement fits a qualified continuous-silicon platform. Neither architecture alone determines a finished device’s speed or price.

  • Bandwidth: compare the memory generation, interface width, transfer rate, and controller.
  • Electrical performance: compare the actual channels and supply network under matching conditions.
  • Cost: include dies, interposer, substrate, assembly, test, qualification, and production volume.
  • Availability: confirm the specific qualified configuration and supply schedule.

Replacing full-area silicon with local silicon changes the material structure, but it does not prove a lower finished-package price. Likewise, a larger interposer may accommodate a different die arrangement without making each connection faster.

A useful cost comparison is total build and test cost divided by the number of passing packages. Less full-area silicon is only one input. Bridge integration, substrate complexity, assembly losses, and the value of attached logic and HBM can outweigh that saving. Compare the same functional target and production assumptions, not unlike products.

For electrical comparison, use extracted channel resistance, capacitance, loss, and crosstalk at the intended data rate. A short but congested route is not automatically better than a longer route with a better reference environment. For thermal comparison, hold workload, cooling conditions, and temperature limits constant.

Design Situation Architecture to Evaluate
Existing die set fits a qualified silicon-interposer floorplan S, against its routing, power, and thermal limits
Integration area exceeds the published S offering L, with confirmed bridge map and qualified size
Dense connections concentrated at neighboring die edges L, if local bridge placement serves those interfaces
Released accelerator already chosen for a board Use its actual package documentation; the board fabricator does not choose its CoWoS variant

CoWoS-S vs CoWoS-L vs CoWoS-R: Where Does R Fit?

CoWoS-R uses an RDL interposer, S uses a silicon interposer, and L combines RDL with embedded local silicon interconnects.

Variant Interposer Approach
CoWoS-S Full silicon routing platform
CoWoS-R Polymer-and-copper RDL platform
CoWoS-L RDL platform with local silicon interconnects

CoWoS-S vs CoWoS-R compares silicon-based and RDL-based interposers. CoWoS-L vs CoWoS-R focuses on the local silicon interconnects added to L’s architecture. R should not be treated as merely another name for L.

Routing figures must stay attached to the relevant variant. A published RDL line-and-space value for R is not automatically the wiring pitch of an S interposer or an L silicon bridge.

CoWoS-L vs EMIB: Are They the Same?

CoWoS-L and Intel EMIB both use local silicon interconnect concepts, but the bridge integration is different: L embeds LSI in its interposer platform, while EMIB embeds a bridge in the package substrate.

That difference affects the surrounding interconnect architecture and design flow. The technologies are not interchangeable components or identical manufacturing processes. Intel also offers multiple EMIB generations, so a feature of one version should not be attributed to the entire family. See Intel’s advanced packaging overview for its current platform descriptions.

What Should a PCB Designer Compare?

A PCB designer should compare the released components’ footprints, power requirements, external interfaces, and mechanical limits—not select a board stackup from the CoWoS letter.

Distinct semiconductor, interposer, package substrate, and system PCB integration levels
  • Footprint: ball map, land pattern, escape routing, and keep-outs.
  • Power: supply rails, current demand, and decoupling requirements.
  • Signals: interface specifications, reference planes, and channel models.
  • Mechanics: package support, cooling attachments, and board constraints.
  • Assembly: component handling, soldering profile limits, and inspection requirements.

Our guide to advanced HDI PCBs covers board-level routing options. For the broader semiconductor context, our TSMC overview separates foundry technology from the finished electronic system.

FAQ About CoWoS-S vs CoWoS-L

Can the same PCB accept S and L packages interchangeably?

Only if the actual components are specified as compatible. Matching the CoWoS family does not establish a common ball map, dimensions, supply rails, signal assignment, or cooling requirement.

Does CoWoS-L always support more HBM than CoWoS-S?

No. A larger available platform can accommodate a more expansive die arrangement, but HBM count is also limited by the processor interfaces, memory configuration, routing, power, and cooling design.

Does CoWoS-S have to be replaced in every new design?

No. A qualified S implementation can remain suitable if it meets the required integration area and electrical, thermal, and manufacturing targets. A newer packaging option is not by itself a reason to redesign a working product.

Can CoWoS-S and CoWoS-L use the same memory generation?

Yes, the architecture name does not uniquely identify the HBM generation. Compatibility must be established for the specific logic, memory, and package implementation rather than inferred from S or L.

Is CoWoS-L the same technology as SoIC?

No. CoWoS-L connects dies through an interposer platform. SoIC is a die-stacking technology; a stacked die assembly can subsequently be integrated into a larger package. They address different integration levels.

Does either option require a fixed PCB layer count?

No. PCB layer count follows the external ball map, routing density, power distribution, channel requirements, and manufacturing rules. Interposer metal layers are not motherboard layers, so they cannot be converted into a PCB stackup count.

How Can We Help with the Surrounding PCB and PCBA?

At EBest Circuit, we provide PCB fabrication and PCBA services. For a design using an advanced package, we review the board files, stackup, and assembly scope against the actual component requirements. We do not equate these services with manufacturing CoWoS interposers.

Send your Gerber files, package information, quantities, and stackup requirements to sales@bestpcbs.com. Include the BOM and test requirements for assembly so we can discuss a board-level manufacturing solution.

You may also like

PCB Silicon Powder Application Percentage: How Much Silica Filler Is Used?

September 24th, 2026

PCB silicon powder application percentage does not have one universal value. In PCB laminate discussions, “silicon powder” usually means electrically insulating silica powder (SiO2) used as a resin filler, not elemental silicon (Si). Published PCB material formulations range from low additions measured in parts per hundred resin to highly filled dielectric systems above 50 wt%, but those figures use different calculation bases and cannot be compared until the denominator is known.

PCB silicon powder application percentage illustrated with silica powder, epoxy resin, glass cloth and copper-clad laminate

What Does PCB Silicon Powder Mean?

In this context, PCB silicon powder is an imprecise trade expression. The functional filler in most copper-clad laminate and PCB insulation formulas is silica, silicon dioxide or SiO2. Suppliers may describe it as fused silica, spherical silica, crystalline silica, amorphous silica or surface-treated silica, depending on its structure and processing.

Silica powder is mixed into a thermosetting or thermoplastic resin system before the material becomes prepreg, a resin-coated film or another dielectric layer. It can change thermal expansion, stiffness, resin flow, moisture response, drilling behavior and electrical performance. The correct percentage therefore depends on the laminate family and the property balance required.

Is It Silicon or Silica in PCB Materials?

Elemental silicon and silica are not interchangeable. Elemental silicon is the semiconductor material used for integrated circuits, power devices and wafers. Silica is an electrical insulator and a common mineral filler. A document that says only “silicon powder” should be checked against the chemical name, formula and safety data sheet before it is used for material selection.

Comparison of elemental silicon and silica filler used in PCB laminate resin
Term Chemical identity Typical PCB-related role Do not confuse it with
Silicon Si Semiconductor dies, wafers and selected electronic materials White insulating filler in laminate resin
Silica SiO2 Inorganic filler in dielectric resin systems Conductive or semiconducting silicon powder
Silicone Siloxane polymer family Coatings, adhesives, gels and encapsulants Silica powder or silicon wafer material

The long-tail expression PCB silica is also ambiguous. It may refer to silica-filled laminate resin, quartz-rich material, or simply a spelling shortcut. For a fabrication drawing or material approval, use the exact resin system and laminate grade rather than this shorthand alone.

What Is a Typical PCB Silicon Powder Application Percentage?

A defensible answer is a range tied to a formulation basis, not a single industry-wide target. Published PCB-related formulations show examples from roughly 5–70 wt% siliceous filler in a complete thermosetting resin composition, approximately 12.5–20 parts silica per 100 parts epoxy resin in another system, and about 50–70 mass% silica relative to the dielectric portion of certain silica-filled PTFE composites. Other insulating resin systems report inorganic filler ranges around 50–80 wt%.

These are formulation examples, not universal purchasing specifications. They may describe different resin chemistries, particle treatments, reinforcement contents and final products. A percentage that works for one low-loss PTFE dielectric cannot be copied directly into an FR-4 epoxy-glass laminate.

Published expression What the denominator may be How it should be interpreted
5–70 wt% siliceous filler Complete thermosetting resin composition Broad formulation window; not a finished-board standard
12.5–20 parts per 100 parts epoxy Epoxy resin only A phr-style recipe cannot be read as final laminate wt%
50–70 mass% silica Dielectric portion of a filled PTFE system Relevant to that dielectric architecture, not generic FR-4
50–80 wt% inorganic filler Specified insulating resin composition May include formulation-specific adhesion and flow limits

Which Percentage Basis Is Being Reported?

Before comparing two data sheets, identify the numerator and denominator. “30% silica” can mean 30 wt% of the mixed resin composition, 30 wt% of resin solids, 30 vol% of the dielectric, or 30 parts per 100 parts resin. Glass cloth, solvents, curing agents and copper may be included in one calculation and excluded from another.

Mass and volume measurement bases used to report silica filler percentage
  • wt% of resin composition: filler mass divided by the mass of the specified mixed resin system.
  • wt% of resin solids: volatile solvent is excluded, but curing agents and modifiers may be included.
  • phr: filler parts by mass per 100 parts of a named resin component; it is not automatically a percentage.
  • vol%: volume fraction; conversion from wt% requires material densities.
  • final laminate wt%: may include glass reinforcement and sometimes other constituents, so it differs from the resin recipe.

If the basis is missing, the percentage is incomplete. Ask for the test or formulation definition before using it in a stack-up comparison.

Why Does the Silica Filler Percentage Vary?

Resin chemistry sets the first boundary. Epoxy, modified epoxy, cyanate ester, hydrocarbon and PTFE systems have different viscosities, cure mechanisms and filler compatibility. The same mass of silica can produce very different flow and adhesion behavior in those matrices.

Particle shape and size distribution also change the practical loading. Spherical particles can pack and flow differently from irregular ground particles. A blended particle-size distribution may reduce void space, while an unsuitable distribution can increase viscosity or leave poor surface quality. Surface treatment affects how the particles wet and bond to the resin.

The target dielectric constant, dissipation factor, thermal expansion, modulus, moisture absorption, bond strength and drillability must be balanced together. That is why the phrase silica filler should lead to a material-system review, not a percentage-only decision.

How Is Silica Used in FR-4 and Copper-Clad Laminates?

In an epoxy-glass copper-clad laminate, the dielectric is not simply resin plus powder. Woven glass cloth provides reinforcement, the resin fills the weave and bonds the structure, and copper foil forms the conductive layers. The PCB laminate silica filler content belongs to the resin formulation and influences how the prepreg flows, fills copper features and cures during lamination.

Silica-filled epoxy resin, glass cloth, prepreg and pressed copper-clad laminate

For conventional FR-4 PCB manufacturing, we select and process an approved laminate grade rather than inventing a silica ratio at the PCB fabrication stage. The laminate supplier controls the resin recipe; our job is to confirm the material designation, stack-up, thickness, copper weight, electrical requirements and process compatibility.

How Much Silica Is Used in High-Frequency PCB Laminates?

High-frequency materials may use substantial mineral loading to tune dielectric properties, dimensional stability and thermal expansion. Some silica-filled PTFE composites disclose silica contents around 50–70 mass% of the dielectric in specific formulations. Hydrocarbon or modified resin systems can use different filler packages and calculation bases.

Do not choose an RF PCB material from filler percentage alone. Dk, Df, frequency, test method, copper roughness, glass style, thickness tolerance and moisture behavior matter together. Two laminates with similar silica content can produce different insertion loss and fabrication behavior.

What Properties Change as Silica Content Increases?

More silica often lowers the effective thermal expansion of the resin-rich portion and increases stiffness. It can also reduce resin shrinkage and help dimensional stability. However, the outcome depends on silica type, particle geometry, treatment, dispersion and the base polymer.

Property Possible effect of higher silica loading What must still be verified
CTE Often decreases in the filled resin Measured laminate-axis CTE and temperature range
Modulus Often increases Peel strength, brittleness and thermal-cycle reliability
Resin flow Usually becomes more restricted as viscosity rises Copper fill, glass wet-out and lamination window
Dielectric behavior Dk and Df may shift Frequency-specific data and actual construction
Drilling Tool wear and hole-wall quality may change Drill parameters, smear control and reliability
Moisture response Can improve in a suitable formulation Complete resin system and conditioning method

These are tendencies, not guarantees. Filler percentage without the measured laminate data cannot establish finished-board performance.

How Do Particle Shape, Size and Surface Treatment Affect Loading?

Fine particles increase surface area and can raise viscosity quickly. Larger particles may reduce viscosity at the same mass loading but can create different surface and spacing constraints. Spherical silica is often selected when high loading and manageable flow are both important; irregular particles may interact differently with the resin and reinforcement.

Surface treatment improves compatibility between inorganic particles and the organic resin. Poor treatment or dispersion can cause agglomeration, voids, weak interfaces or inconsistent dielectric behavior. Therefore, “40% silica” is not a complete material description unless particle morphology, distribution and treatment are also controlled.

What Happens When the Filler Percentage Is Too High or Too Low?

If filler is too low for the intended system, thermal expansion and cure shrinkage may remain higher than desired, and the dielectric may miss its dimensional or electrical target. If filler is too high, viscosity can restrict resin flow and glass wet-out, reduce adhesion, increase brittleness, complicate drilling or make fine-feature filling less reliable.

The optimum level is therefore a processing window. It must support lamination and copper adhesion while delivering the required thermal and dielectric properties. This is especially important for dense multilayer constructions, heavy copper areas and small via structures where resin movement is limited.

Can PCB Buyers Specify a Silica Percentage?

A buyer can specify silica content when a controlled material specification, regulatory requirement or validated product design genuinely depends on it. For most PCB orders, however, the stronger approach is to specify the approved laminate grade and the performance requirements that the board must meet.

Useful procurement fields include laminate manufacturer and grade, Tg, decomposition temperature, z-axis CTE, Dk/Df test method and frequency, thickness tolerance, copper type, UL status, moisture performance and any material declaration. For thermal exposure, a suitable High-Tg PCB material should be selected from the full data set, not from the silica number alone.

If a custom resin formulation is mandatory, identify whether the requested value is wt%, vol% or phr and whether it applies to resin solids, dielectric or final laminate. Also define the verification document, because routine PCB incoming inspection normally confirms the laminate grade and certificate rather than reverse-engineering its proprietary filler recipe.

What Should You Confirm With a PCB Manufacturer?

Send the PCB manufacturer the laminate grade, stack-up, finished thickness, copper weights, impedance requirements, operating temperature, thermal cycles, frequency range and any restricted-material requirement. If silica content is a controlled characteristic, include the exact basis and acceptance document.

  • Is “silicon powder” actually Si, SiO2 or a silicone-based material?
  • Does the percentage use wt%, vol% or parts per hundred resin?
  • Does the denominator include glass cloth, curing agents, solvent or the final laminate?
  • Which laminate grade and revision provide the required property data?
  • Are the Dk/Df values measured at the frequency and by the method used in the design?
  • Will the chosen resin flow and filler system support the copper geometry and lamination stack?

At EBest Circuit (Best Technology), we review the material callout together with the stack-up and fabrication requirements. Email the controlled drawing and laminate specification to sales@bestpcbs.com. For a PCB silicon powder application percentage requirement, we will first confirm the material identity and calculation basis before assessing manufacturability.

You may also like

Turnkey PCB Assembly Services at EBest Circuit

September 23rd, 2026

Turnkey PCB assembly combines bare-board fabrication, component procurement, assembly, and agreed inspection and testing in one managed order. At EBest Circuit, we coordinate these stages from your released design files, so your team does not have to separately manage a PCB fabricator, parts supplier, and assembly shop. We support SMT, through-hole, and mixed assemblies, from prototypes to production. Our engineering review checks whether the PCB data, BOM, component footprints, and assembly instructions agree before purchasing and production proceed. Send us your files, quantities, and test requirements for a project-specific quotation.

Turnkey PCB assembly combining PCB fabrication, component sourcing, assembly and testing

Key Takeaways

  • Our turnkey PCB assembly services bring PCB fabrication, component sourcing, assembly, and agreed testing into one project.
  • We support SMT, through-hole, and mixed assemblies. Standard FR-4 fabrication includes 1–10 layers, with high-Tg material required for 8 layers and above.
  • Alternative components require your approval before they are introduced into the build.
  • Our no-MOQ assembly service, DFM/DFA review, and online WIP updates support prototype builds and production planning.
  • Our inspection equipment includes 3D SPI, 3D AOI, and X-ray. Functional testing needs a defined test procedure and acceptance limits.
  • Price and delivery depend on the BOM, PCB construction, assembly complexity, quantity, and test scope.
  • Send your Gerber files and BOM for a quotation, or share the files you have for an initial discussion if the design is still in progress.

What Does Our Turnkey PCB Assembly Service Include?

We can manage the bare PCB, purchased components, board assembly, and the inspection and testing agreed in your order. Our PCB assembly service can also include programming and additional integration work when specified in the quotation.

Service stage Our scope
PCB fabrication FR-4 PCB, Multilayer PCB, HDI PCB, Heavy Copper PCB, Metal-Core PCB, Ceramic PCB, Flexible PCB, Rigid-Flex PCB, High-Frequency PCB, High-Tg PCB
Component sourcing BOM Review, Authorized-Channel Procurement, Component Availability Checks, Alternative Part Proposals, Incoming Component Inspection, Customer-Supplied Parts Coordination
PCB assembly SMT Assembly, Through-Hole Assembly, Mixed-Technology Assembly, BGA Assembly, Flex PCB Assembly, Ceramic PCB Assembly
Inspection and testing First-Article Inspection, 3D SPI, AOI, X-Ray Inspection, Visual Inspection, Functional Testing
Additional integration Programming, Custom Wire Harnesses, Enclosure Assembly, Box Build Assembly, System Integration

Full turnkey means we source the boards and components. In partial turnkey, you supply selected parts while we procure the remainder. Consigned assembly uses customer-supplied materials. We confirm responsibility for each item before the order is released, including extra components needed for setup and handling.

Why Choose EBest Circuit for Turnkey PCB Assembly?

Choose EBest Circuit when you need one team to coordinate PCB fabrication, component purchasing, and assembly decisions before production starts. We have provided PCB and PCBA services since 2006, supporting customers from engineering samples through repeat production.

  • Resolve manufacturing questions before committing materials: we review the bare PCB and assembly requirements together. Footprint, panelization, and soldering questions can be addressed before boards are fabricated and components are purchased, helping avoid a board revision after materials have already been ordered.
  • Keep control of component substitutions: our purchasing team checks authorized-channel availability and proposes alternatives when needed. Your engineers approve changes before use, so a purchasing decision does not silently change the circuit, footprint, or firmware requirements.
  • Start with the quantity your design needs: our no-MOQ assembly service supports engineering samples without requiring a production-sized order. Setup, tooling, component pack sizes, and material minimum purchases remain visible in the quotation.
  • Define how the build will be checked: we coordinate first-article inspection, SPI, AOI, X-ray, and the agreed functional tests. Your team can specify which measurements and records are needed for acceptance, rather than relying on an undefined claim that the boards are “tested.”
  • Follow progress through one contact: online work-in-progress (WIP) updates and one-to-one sales support help you track production and resolve outstanding material or engineering questions without chasing separate suppliers.
  • Extend the order beyond the PCBA: custom wire harnesses, enclosure assembly, and box build can be quoted with the board. This lets you define the wiring, programming, and final integration requirements in the same project.

For supplier qualification, our certification portfolio includes ISO 9001:2015, ISO 13485:2016, IATF 16949, and AS9100D. Request the current certificate and applicable manufacturing-site scope for your project.

Have a BOM shortage or an assembly question? Email the available files and your main concern to sales@bestpcbs.com. We can review component availability, manufacturing requirements, and the testing scope with you before you finalize the order.

As your turnkey PCB assembly manufacturer, we connect these services to a defined build: approved materials, released files, agreed inspection coverage, and a clear delivery scope. Our full turnkey PCB assembly overview explains the sourcing responsibilities when comparing full and partial turnkey orders.

Which PCB Types and Component Packages Can We Assemble?

We support SMT, through-hole, and mixed-technology assemblies, including boards with BGA devices. We review package geometry, board construction, and component temperature limits before confirming the process.

SMT, through-hole and mixed PCB assembly options
  • SMT: surface-mount passives, ICs, and connectors are placed onto printed solder paste and reflowed.
  • Through-hole: leaded connectors, relays, transformers, and other inserted components require a suitable soldering and inspection route.
  • Mixed assembly: we plan the SMT and through-hole sequence together, accounting for component access and exposure to subsequent soldering operations.
  • Flexible and specialty boards: support fixtures, thermal behavior, and handling requirements need review rather than assuming the same process as a rigid FR-4 board.

A package name alone is insufficient for approval. Include the exact manufacturer part number and package drawing, especially for bottom-terminated devices, fine-pitch connectors, and components with unusual mounting or thermal-pad requirements.

PCB fabrication capabilities supporting your PCBA: the values below distinguish our standard FR-4 process from special-process options. They describe bare-board fabrication, not guaranteed assembly limits.

FR-4 parameter Standard process Special process, subject to engineering review
Layer count 1–10 layers; high-Tg material for 8 layers and above 10–32 layers
Inner-layer line width/spacing 4/4 mil at 0.5 oz and 1 oz copper 3/3 mil at 0.5 oz and 1 oz copper
Outer-layer line width/spacing 4/4 mil at 1 oz copper 3/3 mil at 1 oz copper
Minimum finished mechanical hole 0.20 mm 0.15 mm
Maximum through-hole aspect ratio 8:1 10:1

Our standard high-Tg material options include ITEQ IT180, Shengyi S1000-2, and KB6167. Final material selection and routing limits depend on the specified copper weight, stack-up, dimensions, and fabrication requirements. Do not combine the smallest hole, finest trace, and highest layer count into one assumed process window.

Assembly and material-handling options:

  • Reels, cut tape, tubes, trays, and loose components can be reviewed for the build. Packaging and supplied quantities affect feeder setup and handling.
  • Our published fine-pitch capability includes 01005 components and 0.25 mm BGA pitch. These are advanced requests requiring engineering confirmation of the actual package, pad design, PCB construction, stencil, and inspection plan before order acceptance.
  • We support FR-4, HDI, metal-core, ceramic, flexible, and rigid-flex PCB projects, with fixtures and soldering conditions selected for the substrate.

How Do We Manage Component Sourcing and BOM Changes?

We source against the approved BOM and ask you to confirm proposed alternatives before purchasing a substituted component. Our sourcing channels include component manufacturers and authorized distributors such as DigiKey, Mouser, Arrow, and Avnet.

BOM review covering part-number matching, alternatives and customer approval before purchase

A purchasing-ready BOM identifies the manufacturer, full part number, quantity per board, reference designators, and any approved alternatives. Mark do-not-populate positions clearly. For customer-supplied components, identify the supplied quantities and packaging.

When a part is unavailable, our review should address more than its nominal value. A replacement resistor may differ in power rating or size; a connector may have a different mating interface; an IC may need firmware changes. We return the proposed substitution for engineering approval and use the approved BOM revision for the build.

What Do We Check Before PCB Assembly?

We check agreement between the fabrication files, BOM, placement data, and assembly drawing, then review the features that affect placement, soldering, inspection, and testing.

  • Footprints and orientation: package dimensions, pin 1, diode and capacitor polarity, connector orientation, and reference designators.
  • Board and panel details: fiducials, tooling features, component-to-edge clearance, breakaway areas, and handling support.
  • Soldering details: stencil openings, thermal-pad paste coverage, solder-mask clearances, and components that need a special assembly sequence.
  • Inspection and test access: visible joints, hidden joints requiring X-ray, programming headers, and accessible test points.
  • Document consistency: matching PCB and BOM revisions, intentional unpopulated positions, and unambiguous assembly notes.

If the layout still needs work, our PCB design support can help address manufacturing questions before the release. DFM identifies production issues; it does not replace validation of the circuit’s electrical design.

How Does Our Turnkey PCB Assembly Process Work?

Our process moves from file review and quotation to material preparation, assembly, inspection, agreed testing, and shipment. Engineering questions and substitutions are resolved before the affected stage proceeds.

Our SMT equipment includes the GKG-GLS stencil printer, Yamaha YSM20R placement machine, and Suneast SER710NH nitrogen reflow oven. Nitrogen reflow provides a controlled soldering atmosphere for the selected process. Through-hole work can use the Suneast E-FLOW-610 wave soldering system where the board and component arrangement are suitable.

Turnkey PCB assembly workflow from file review through boards and parts, assembly, inspection and test
  1. Review your files: identify missing data, manufacturing questions, quantities, and test requirements.
  2. Confirm the quotation: agree on the PCB specification, procurement responsibility, assembly scope, schedule, and deliverables.
  3. Prepare boards and components: fabricate the PCB and procure the approved BOM, then check incoming materials against the order.
  4. Set up and assemble: prepare the stencil, placement program, soldering process, and first-article checks before continuing the batch.
  5. Inspect and test: apply the agreed process inspections, programming, and electrical or functional tests.
  6. Release and ship: complete the agreed records and packaging requirements for delivery.

This turnkey PCB manufacturing workflow allows procurement and fabrication to be coordinated, but the delivery date still depends on material availability and resolution of open technical questions.

How Do We Inspect and Test Your PCB Assemblies?

We use solder-paste inspection, optical inspection, and X-ray where applicable, then perform the electrical or functional testing defined for your project. Each method checks a different part of assembly quality.

Our inspection equipment includes SINIC-TEK S8080 3D SPI, JCX830 first-article inspection, SINIC-TEK A510DL 3D AOI, and UNICOMP AX8200 X-ray. First-article checks verify the initial setup before the batch continues; SPI checks printed paste before placement, while AOI and X-ray address visible and hidden assembly features. This staged approach gives us opportunities to identify setup and soldering issues before final testing.

PCB assembly quality checks using SPI, AOI, X-ray and functional test
Method Primary check
3D SPI Solder-paste deposits after printing, including volume, height, and position.
AOI Visible placement and soldering defects, such as missing components, misalignment, and visible bridges.
X-ray Hidden solder-joint features, including selected BGA connections and voiding.
Electrical or functional test Specified circuit behavior against agreed inputs, outputs, and pass/fail limits.

An AOI or X-ray pass does not prove that the complete product functions correctly. For functional testing, provide the test procedure, supply conditions, firmware version, connections, and acceptance limits. Confirm whether fixtures, loads, programming equipment, or a known-good sample are needed during quotation.

For example, a power-control board may require checks of startup current, output voltage, and operation under a defined load. These limits must come from the product specification, not a generic assembly checklist.

Can We Support Both Prototypes and Production Orders?

Yes. We support no-MOQ prototype assembly, small batches, and production orders, with procurement and setup planned around the quantity and design maturity. Our PCB prototype service can support the bare-board stage of an assembled prototype project.

For a prototype, prioritize correct component selection, access for measurements, programming, and the tests needed to evaluate the design. Before a production repeat, release the final PCB files, BOM, assembly instructions, and firmware together. Tell us whether changes from the prototype affect the test fixture, component sourcing, or approved assembly process.

For repeat orders, we review current component availability and the released revision rather than assuming the previous purchasing conditions still apply.

What Determines Turnkey PCB Assembly Cost and Lead Time?

Cost is driven by the PCB specification, purchased components, assembly work, setup, inspection, and testing. Lead time is often constrained by the longest-lead component or a special PCB material, rather than placement time alone.

  • PCB construction: layer count, material, copper weight, dimensions, surface finish, and special features.
  • Components: exact part numbers, availability, order quantities, packaging, and approved sourcing channels.
  • Assembly: placement count, double-sided processing, through-hole work, package complexity, and fixtures.
  • Testing: programming, test development, fixtures, test duration, and required records.
  • Order quantity: setup costs are spread across the batch, while component purchasing breaks can change the unit price.

To evaluate options, send a prototype quantity and expected production quantities together. We can quote the defined builds and discuss approved alternatives where sourcing is a constraint. We confirm delivery after reviewing files and current material availability; we will include the confirmed schedule in your quotation.

FAQ About Turnkey PCB Assembly

What is the turnkey PCB assembly meaning in a quotation?

It means the supplier manages the agreed board fabrication, component sourcing, and assembly scope. Check the quotation for testing, programming, shipping, and integration items, because these are not automatically identical across suppliers.

Can I supply an expensive or pre-programmed component?

Yes. A partial-turnkey order can combine your supplied components with parts we purchase. Confirm quantities, packaging, handling requirements, and responsibility for replacement parts before shipment.

Will you change an unavailable component without asking?

Proposed alternatives should be approved by your team before use. Provide an approved-vendor or alternative-part list when you want us to purchase from prequalified options.

Is box build automatically included?

No. Enclosures, cables, wiring, mechanical assembly, and system-level testing must be specified and quoted. A completed PCBA is not necessarily a finished enclosed product.

Can you quote before every design file is final?

We can review the available information for a preliminary quotation. Final pricing and production release require the agreed manufacturing files, BOM, quantity, and test scope.

Does a certified quality system make my product certified?

No. A manufacturer’s quality-system certification does not replace product-specific approvals or compliance testing. Tell us the documentation and product requirements that apply to your project.

Request a Turnkey PCB Assembly Quote from EBest Circuit

Send your Gerber files and BOM to sales@bestpcbs.com. We can review the PCB construction, component availability, assembly requirements, and testing scope, then prepare a quotation for the agreed build.

Ready for a quotation? Include the following where available:

  • Gerber files and PCB fabrication specifications.
  • BOM with manufacturer part numbers, quantities, reference designators, and approved alternatives.
  • Pick-and-place data and assembly drawings.
  • Prototype or production quantity, target delivery date, and customer-supplied components.
  • Programming, testing, inspection-record, and box-build requirements.

Design still in progress? Send the files you have and tell us what needs to be resolved, such as a hard-to-source component, a fine-pitch package, or a prototype assembly requirement. You do not need a complete production package to start the discussion. Final pricing and production release will require the agreed files and specifications.

Our review will help identify missing information, procurement questions, and manufacturing or test requirements that affect the quotation. Tell us whether you need PCB fabrication and assembly only or a wider scope including programming, wire harnesses, and enclosure integration.

You may also like

What Does OL Mean on a Multimeter? Causes and Fixes

September 23rd, 2026

What does OL mean on a multimeter? In most cases, OL tells you that the meter cannot display a normal numeric result under the present test conditions. In resistance and continuity modes, it usually means an open circuit or a resistance above the available range. In voltage or current mode, it more often means the measured value exceeds the selected range. The exact interpretation depends on the function, range, lead ports, probe contact, and meter model.

OL is therefore an indication, not a complete diagnosis. It can be perfectly normal when the probes are separated, useful evidence of a broken connection, or a warning that the selected range is too low. This guide shows how to read it by mode and how to isolate the cause without creating a new fault.

Digital multimeter displaying OL while probes test an open PCB trace

What Does OL Mean on a Multimeter?

Meter manufacturers use OL as a compact display message for conditions such as overload, over limit, or a value outside the present measurement range. When checking resistance or continuity, the same display commonly corresponds to an open path or effectively infinite resistance. The manual for your meter remains the final reference because display conventions and test thresholds vary.

Meter mode What OL usually means First check
Resistance (Ω) Open circuit or resistance above the selected/measurable range Power off, probe contact, range, and component isolation
Continuity No conductive path below the meter’s continuity threshold Broken wire, open fuse, switch state, trace, or connector
Diode test Reverse bias, open junction, poor contact, or voltage drop beyond the test limit Probe polarity and a second reading with probes reversed
Voltage Input above the selected range, especially on a manual-ranging meter Correct AC/DC function, ports, and a safely higher range
Current Current above the selected range or an invalid measurement setup Correct jack, fuse, series connection, and current rating

Do not treat OL as proof that a part has failed until you confirm the selected mode and repeat the test correctly. A separated probe, oxidized terminal, lifted PCB pad, open via, blown fuse, or simply the wrong range can all produce the same two letters.

What Does OL Mean on a Multimeter When Measuring Resistance?

When people ask what does OL mean on a multimeter when measuring resistance, the practical answer is: the meter sees more resistance than it can show on the current range. With the probes separated, this is expected because there is no conductive path between them. Across a component or conductor that should be connected, OL suggests an open path, poor probe contact, or an out-of-range resistance.

Multimeter in resistance mode showing OL across an open circuit

Before measuring resistance, disconnect power and discharge capacitors. Fluke’s resistance guidance notes that an unconnected meter can normally show OLΩ and that the component may need to be isolated from parallel circuit paths for a meaningful result. In-circuit measurements can be affected by other resistors, semiconductors, contamination, and stored charge.

Use this sequence:

  1. Turn the circuit off and verify it is de-energized.
  2. Discharge capacitors using an appropriate safe procedure.
  3. Put the black lead in COM and the red lead in the V/Ω jack.
  4. Select Ω and, on a manual-ranging meter, begin with a higher range.
  5. Touch the probes together. A low reading confirms that the meter and leads can complete a path.
  6. Measure the component or conductor with clean, firm probe contact.
  7. If OL remains, isolate one end of the component or divide the circuit into sections.

A resistor that is intentionally above the meter’s range can also display OL even though it is not electrically open. Check the resistance value, expected tolerance, and the meter specification before condemning the part.

What Does OL Mean on a Multimeter When Measuring Continuity?

For what does OL mean on a multimeter when measuring continuity, OL normally means the tested path does not meet the meter’s continuity threshold. In plain terms, the path is open or too resistive for the beeper to recognize as continuous. Klein Tools’ MM400 instructions, for example, state that an open circuit displays OL in continuity mode.

Comparison of OL with no continuity and a low-resistance continuity reading

Continuity mode is useful for finding opens in:

  • Wires, cables, and connectors
  • Fuses and closed switches
  • PCB traces, plated through-holes, and vias
  • Solder joints and jumper links
  • Ground paths that should be directly connected

No beep does not always mean absolute infinite resistance. Each meter has a model-specific beep threshold. A path with tens or hundreds of ohms may be electrically connected yet remain above that threshold. Switch to resistance mode when you need a numeric value rather than a quick pass/fail indication.

For PCB troubleshooting, begin at two known points on the same net and then shorten the distance between probes. This divide-and-test method helps locate an open trace, cracked via, damaged connector, or suspect solder joint. For production-level context, see our overview of PCB testing methods.

What Does OL Mean on a Multimeter When Measuring Voltage?

If you search what does OL mean on a multimeter when measuring voltage, the most common explanation is an over-range condition. The input is above the selected voltage range, or the meter is on the wrong function. An auto-ranging meter usually changes range automatically, while a manual-ranging model requires you to select a range above the expected value.

Manual-ranging multimeter changing from OL to 24.0 volts after selecting a higher range

Check these items before re-measuring:

  • Select DC voltage for DC supplies and batteries, or AC voltage for AC sources.
  • Keep the black lead in COM and the red lead in the voltage/ohms jack.
  • On a manual-ranging meter, start at a range above the maximum expected voltage.
  • Confirm the meter, probes, and accessories carry the required voltage and CAT rating for the environment.
  • Stop if the source may exceed the instrument’s maximum input rating.

Never solve a voltage OL by moving the red lead to a current jack. The current input is a low-resistance path intended for a series connection. Placing it directly across a voltage source can blow the meter fuse, damage equipment, or create an arc hazard.

What Does OL Mean in Current and Diode Modes?

In current mode, OL can indicate that current exceeds the selected range. Current must be measured with the meter connected in series, using the correct fused input and function. If you do not know the expected current, begin with the highest suitable range and follow the meter manufacturer’s instructions. Do not place a meter in current mode directly across a power source.

In diode mode, an OL reading can be normal in one direction because a healthy diode blocks reverse current. A typical test checks both polarities:

  • A normal silicon diode generally shows a forward-voltage reading in one direction and OL in the reverse direction.
  • OL in both directions can indicate an open diode, poor contact, an in-circuit parallel path issue, or a junction outside the meter’s test capability.
  • A very low reading in both directions can indicate a shorted diode.

These patterns are diagnostic clues, not universal acceptance limits. Package type, device technology, circuit connections, and meter test voltage all matter. Our rectifier diode guide explains how diode behavior relates to PCB power paths.

How Do You Fix an Unexpected OL Reading?

There is no single “OL fix.” The goal is to determine whether the display is expected for the selected mode or caused by the setup, test point, or circuit.

  1. Read the mode first. Resistance, continuity, diode, voltage, and current modes interpret OL differently.
  2. Check the lead ports. For resistance, continuity, diode, and voltage measurements, the red lead normally belongs in the V/Ω input, not the current jack.
  3. Confirm the range. Increase the range on a manual-ranging meter when measuring a potentially large resistance, voltage, or current.
  4. Verify the leads. In resistance or continuity mode on a de-energized circuit, touch the probes together. A persistent OL can indicate a broken lead, dirty probe tip, loose plug, or faulty meter input.
  5. Improve probe contact. Remove oxidation or flux residue where appropriate and probe clean metal without slipping into adjacent conductors.
  6. Isolate the device. Parallel paths can hide faults or distort readings. Lifting one terminal may be necessary for a reliable component test.
  7. Divide the circuit. Test smaller sections of a wire, PCB net, or connector path until the open location is bounded.
  8. Consult the manual. Confirm the exact display definition, continuity threshold, maximum inputs, and fuse arrangement for that meter.

If the meter displays OL on every resistance and continuity test—including with the probes shorted together—stop troubleshooting the circuit and verify the leads, jacks, battery, fuse where applicable, and meter operation first. A known-good component or test source can help separate an instrument problem from a circuit problem.

How Can You Tell an Open Circuit from an Out-of-Range Reading?

Use the selected function and a controlled change in the test setup. In resistance mode, increase the range or switch to autorange. If a numeric value appears, the original reading was over-range. If OL remains, separate the circuit into smaller sections and verify probe contact. A known open path should remain OL; a valid conductive path should eventually produce a measurable value.

In voltage mode, move to a safely higher voltage range without exceeding the meter’s maximum input. If a numeric voltage appears, OL was an over-range indication. If it does not, recheck AC/DC selection, ports, lead integrity, and the manufacturer’s instructions.

Observation Likely interpretation Next action
OL with probes separated in Ω mode Normal open-circuit indication Touch probes together to verify the measurement path
OL becomes a number on a higher range Previous range was too low Use the range that resolves the value safely
OL remains across a conductor that should be continuous Open path, poor contact, or bad lead Verify leads, then divide the conductor into sections
OL in one diode direction only May be normal reverse bias Compare the forward reading with the device specification

When you need more than a pass/fail reading—such as resistance, capacitance, or inductance across components—an LCR meter may provide a more suitable test method than a basic continuity check.

What Safety Checks Matter Before Troubleshooting OL?

Resistance, continuity, diode, and capacitance tests generally apply an internal meter signal and should be performed on a de-energized circuit. Official Fluke and Klein guidance instructs users to remove power; Fluke also specifies discharging high-voltage capacitors before these tests.

  • Inspect the meter, probes, insulation, and input jacks before use.
  • Confirm the lead locations and selected function before touching the circuit.
  • De-energize and verify the circuit before resistance or continuity testing.
  • Discharge capacitors with a suitable method and confirm the remaining voltage.
  • Use equipment with the correct voltage and CAT rating for the environment.
  • Do not work on hazardous live circuits unless you are trained, authorized, and using an approved procedure and PPE.

For live voltage testing, follow the instrument manual and applicable electrical safety procedures. OL can indicate that you have reached or exceeded a range; it should never be treated as permission to continue beyond the meter’s rated limits.

FAQ About OL on a Multimeter

Does OL always mean the multimeter is overloaded?

No. It can mean over-range, but in resistance and continuity modes it commonly represents an open circuit or a resistance too high to measure. Interpret OL together with the active function and range.

Does OL mean no continuity?

In continuity mode, OL usually means the path is open or above the meter’s beep threshold. A numeric resistance test can show whether a high-resistance path still exists.

Why does the meter show OL before the probes touch anything?

That is normal in resistance or continuity mode. Separated probes form an open measurement path, so the displayed resistance is effectively beyond range.

What does negative OL mean on a multimeter?

A negative OL or minus sign beside OL is model- and mode-dependent. It can indicate an out-of-range negative input or polarity condition. Reduce the input safely, check probe polarity and range, and use the meter manual for the exact definition.

Is OL the same as zero ohms?

No. OL represents extremely high or unmeasurable resistance in Ω mode, while a reading near 0 Ω represents a very low-resistance path. They are opposite conditions.

Does OL mean a fuse is blown?

Across a removed, de-energized fuse, OL in resistance or continuity mode is consistent with an open fuse. Verify the meter and leads first, then confirm the reading at both fuse terminals.

Can a bad test lead cause OL?

Yes. A broken conductor, loose plug, dirty tip, or damaged input jack can keep the measurement path open. Short the probes together in a safe resistance or continuity setup to check the leads.

What Should You Do When OL Points to a PCB Open?

When OL persists across a PCB net that should be continuous, compare the reading with the schematic and layout, then test section by section through connectors, solder joints, traces, vias, and component terminals. Visual inspection alone may miss a hairline trace crack, barrel fracture, or intermittent joint.

At EBest Circuit, we manufacture PCBs and provide PCBA support for designs that require controlled fabrication and assembly checks. If your investigation points to a repeatable open trace, via, or solder connection, send us the Gerber files, stackup, assembly data, and fault location. We can review the manufacturing information and help determine the next practical step before your next build.

You may also like

EMC Meaning in Electronics: EMI, Testing and PCB Design

September 23rd, 2026

The emc meaning in electronics is electromagnetic compatibility: the ability of equipment to work as intended in its electromagnetic environment without creating unacceptable interference for other equipment. In practical terms, an EMC-compatible product controls what it emits and continues operating when exposed to expected disturbances.

EMC is a system-level result, not a single component or PCB feature. Circuit architecture, PCB stackup, return paths, power integrity, cables, shielding, enclosure design, firmware states, and the test setup can all change the result. Engineers therefore need to address EMC during design and verify it against the standards that apply to the finished product.

EMC meaning shown with a PCB under near-field emissions testing

Key Takeaways

  • EMC stands for electromagnetic compatibility, the ability of electronic equipment to operate correctly without causing or suffering unacceptable electromagnetic interference.
  • The purpose of EMC is to let electronic devices coexist reliably by limiting emissions and maintaining immunity in their intended electromagnetic environment.
  • EMC testing checks both emissions and immunity under the standards, operating modes, cable arrangements, and performance criteria applicable to the finished product.
  • In the United States, EMC requirements depend on the product and its functions, so the applicable FCC rules and product standards must be confirmed for each device.
  • EMI risk can be reduced through continuous return paths, compact switching loops, correct decoupling, connector filtering, cable control, shielding, and appropriate enclosure design.
  • EMI and EMC are not interchangeable terms, because EMI is the unwanted electromagnetic disturbance while EMC is the broader goal of controlling emissions and maintaining immunity.

What Does EMC Mean in Electronics?

In electronics, EMC means that a device can coexist with other electrical and electronic equipment in its intended environment. The device must keep its electromagnetic emissions within the applicable limits and maintain acceptable operation when exposed to defined disturbances.

This definition has two complementary sides:

  • Emissions: electromagnetic energy leaving the product through radiation or conductors must remain below the applicable limits.
  • Immunity: the product must continue to meet specified performance criteria when exposed to disturbances such as RF fields, electrostatic discharge, transients, or conducted noise.

The phrase emc meaning in electronics is sometimes reduced to “no interference,” but that is incomplete. Every operating circuit produces electromagnetic energy. EMC engineering controls that energy and its coupling paths so nearby systems can operate together.

Electromagnetic compatibility balancing emissions and immunity

What Is the Difference Between EMC, EMI and EMS?

EMC is the ability to coexist, EMI is the disturbance that causes or may cause a problem, and EMS describes susceptibility to that disturbance. The terms are related, but they are not interchangeable.

Term Full Form Practical Meaning
EMC Electromagnetic compatibility The product limits emissions and tolerates specified disturbances in its intended environment.
EMI Electromagnetic interference Unwanted electromagnetic energy that can degrade or disrupt operation.
EMS Electromagnetic susceptibility The tendency of equipment to be affected by electromagnetic disturbances; immunity expresses resistance to them.

For example, a switching converter can be an EMI source, a cable can provide a coupling path, and a sensitive analog input can be the victim. An EMC design review looks at the complete source-path-victim relationship rather than treating the noise source alone.

What Does EMC Cover: Emissions, Immunity and Coupling?

EMC covers how disturbances are generated, how they travel, and how circuits respond. A useful diagnosis separates the source, coupling path, and victim because changing any one of the three can reduce the problem.

  • Conducted coupling: noise travels through power, ground, signal, or cable conductors.
  • Capacitive coupling: changing electric fields transfer energy between nearby conductors.
  • Inductive coupling: changing magnetic fields induce voltage in an adjacent current loop.
  • Radiated coupling: traces, cables, slots, or enclosures behave as transmitting or receiving structures.
EMC source coupling path and victim relationship in electronic systems

Fast edge rates often matter more than the nominal clock frequency. A low-frequency digital signal with sharp transitions can contain high-frequency energy, while a cable connected to the board can convert common-mode current into radiated emissions.

What Is EMC Testing?

The emc testing meaning is the controlled evaluation of a product’s emissions and immunity against specified limits, test levels, setups, and performance criteria. It is not one universal test; the correct program depends on the product category, intended environment, interfaces, power source, and target market.

If you are asking what is emc testing, the most useful distinction is between pre-compliance and formal compliance work. Pre-compliance measurements help find high-risk frequencies, cables, operating modes, and PCB areas before the final test. Formal testing follows the applicable standard using the required equipment, calibrated setup, distances, limits, and documentation.

Engineer performing a PCB EMC pre-compliance scan with a near-field probe

For a deeper test-oriented overview, see our guide to EMI and EMC testing in PCBs.

Which EMC Tests Are Common for Electronic Products?

Common EMC evaluations include conducted and radiated emissions plus several immunity tests, but not every product needs every test. The applicable product or product-family standard should define the final test plan.

Test What It Evaluates Typical Coupling Path
Conducted emissions Noise returned through power or connected conductors Power leads and cables
Radiated emissions Electromagnetic energy radiated by the product and its cables Enclosure openings, traces, cables, and common-mode currents
Radiated RF immunity Operation under an external radio-frequency field Enclosure, PCB, and cables acting as receiving structures
Conducted RF immunity Response to RF energy coupled onto connected cables Power and signal ports
Electrostatic discharge Response to direct or indirect ESD events Exposed metal, seams, displays, buttons, and connectors
EFT/burst and surge Response to fast repetitive transients or higher-energy events Power and external I/O wiring

Performance criteria also matter. A disturbance may permit no degradation, temporary self-recovery, or controlled operator intervention depending on the applicable standard. Teams should define acceptable behavior before the test instead of deciding after a failure.

Why Do PCBs Cause EMC Problems?

PCBs contribute to EMC problems when fast currents flow through large or discontinuous loops, when noise couples into sensitive nodes, or when common-mode energy reaches an efficient radiator such as a cable. The schematic may be correct while the physical current paths are not.

Frequent board-level causes include:

  • high-speed traces crossing a split or void in the reference plane;
  • large switching-current loops around converters, drivers, or power devices;
  • decoupling capacitors placed too far from IC power and ground pins;
  • long parallel routes that increase crosstalk;
  • filters placed far from the connector where interference enters or leaves;
  • poor shield or chassis termination that forces high-frequency current through signal ground;
  • layer changes without a nearby return-path transition;
  • uncontrolled cable common-mode current.

A PCB is only one part of the final electromagnetic structure. The enclosure, harness, display, power supply, grounding arrangement, connector shells, and installed accessories can turn a small board-level noise source into a compliance failure.

How Can PCB Layout Improve EMC Performance?

PCB layout improves EMC by reducing loop area, preserving continuous return paths, containing high-frequency fields, and preventing noise from reaching external cables. The most effective changes are usually architectural and placement-related, not late additions of random filter components.

PCB EMC layout practices showing return path, ground plane, and connector filtering
  • Route critical signals over a continuous reference plane and avoid plane splits beneath them.
  • Keep switching loops compact and place high-di/dt components close together.
  • Place decoupling capacitors at the relevant power pins with short connections to the reference plane.
  • Keep noisy power sections away from clocks, RF paths, analog inputs, and external connectors.
  • Place filtering and transient protection at the connector boundary.
  • Provide nearby stitching vias when signals change reference layers.
  • Control impedance, return paths, and pair geometry for fast interfaces.
  • Plan shield-can pads, via fences, chassis bonds, and keep-outs before routing is complete.

Our article on the circuit board ground plane explains why return-path continuity and layer references are central to both signal integrity and EMC.

Which Standards and Regulations Apply to EMC?

The applicable EMC requirements depend on the product, environment, interfaces, and market. There is no single “EMC certificate” or universal test list that covers every electronic device.

Common frameworks include the IEC 61000 series for EMC terminology and test methods, CISPR publications for many emissions requirements, FCC rules for relevant radio-frequency emissions in the United States, and the EU EMC Directive for equipment placed on the European market. Product-specific families can add different limits, ports, test levels, operating modes, and performance criteria.

Examples include IEC 61326-1 for certain measurement, control, and laboratory equipment and IEC 60601-1-2 for medical electrical equipment. These examples should not be treated as automatic selections. Confirm the product classification and current edition with the compliance laboratory or responsible regulatory specialist before freezing the test plan.

How Should You Prepare an EMC-Sensitive PCB for Manufacturing?

An EMC-sensitive board should be released with the stackup, reference planes, controlled-impedance requirements, grounding details, shield features, connector interfaces, and assembly notes clearly defined. Fabrication and assembly must preserve the electrical geometry on which the design depends.

Before sending the package, check that it includes:

  • Gerber, ODB++, or IPC-2581 data plus drill and route files;
  • a stackup drawing with materials, finished thickness, and copper requirements;
  • controlled-impedance definitions and coupon requirements where applicable;
  • a released BOM with filter, protection, and shielding components identified;
  • pick-and-place and assembly drawings with polarity and shield orientation;
  • notes for via filling, ground stitching, shield-can pads, and connector-shell grounding;
  • inspection and electrical-test requirements appropriate to the build.

An EMC test is still performed on the finished product or representative system, not on bare Gerber data alone. Manufacturing documentation reduces unintended variation, but it does not replace system-level compliance validation.

FAQ About EMC Meaning

What does EMC stand for in electronics?

EMC stands for electromagnetic compatibility. It describes whether electronic equipment can operate satisfactorily in its intended electromagnetic environment without causing unacceptable interference to other equipment.

Does EMC mean a device produces no EMI?

No. Every active electronic product produces some electromagnetic energy. EMC means emissions remain within the applicable limits and the product has the required immunity for its intended environment.

Is EMC the same as FCC or CE compliance?

No. EMC is the engineering and performance concept. FCC requirements, the EU EMC Directive, and product standards are regulatory or conformity frameworks that may define specific emissions, immunity, documentation, and assessment obligations.

Can a PCB manufacturer certify the finished product’s EMC?

A PCB manufacturer can build the specified stackup, impedance, grounding, shielding pads, and assembly features. Formal product compliance normally requires testing the representative finished equipment under the applicable standard and configuration.

Does a solid ground plane guarantee good EMC?

No. A continuous reference plane usually improves return-path control, but poor connector grounding, large switching loops, cable common-mode current, enclosure seams, or unsuitable filtering can still cause emissions or immunity failures.

Why can a prototype pass while a later version fails?

Changes to the stackup, component substitutions, cable routing, enclosure bonding, firmware modes, clock edges, power supply, or test configuration can change EMC behavior. Revision control should include both electrical design files and the representative test setup.

Is pre-compliance EMC testing worthwhile?

Yes. Near-field scanning and other pre-compliance checks can identify dominant frequencies, noisy PCB regions, cable effects, and operating modes before formal testing. They reduce risk, but they do not replace the required compliance test.

How Can EBest Circuit Support an EMC-Aware PCB Build?

EMC performance begins with system design, while consistent PCB fabrication and assembly help preserve the intended stackup, return paths, impedance geometry, grounding features, and shielding interfaces. At EBest Circuit, we support PCB fabrication and PCBA from prototype through volume production using the released manufacturing data and agreed inspection scope.

For projects involving industrial interfaces, power conversion, fast digital links, or shielded connectors, our industrial network PCB design checks provide a useful release reference. Send your Gerber files, stackup, BOM, assembly data, quantities, and EMC-related manufacturing notes to sales@bestpcbs.com for engineering review and a quotation.

You may also like