PCB manufacturing PCB manufacturing
Home > Blog

solder wicking

Thermal Via Solder Wicking: Protect the QFN Pad Joint
Monday, November 9th, 2026

Thermal via solder wicking happens when molten solder enters a via opening connected to a package’s exposed land. On a power QFN, that can reduce solder remaining under the package or leave solder on the opposite side. Prevent it by deciding together which vias remain open, where paste is printed and what the assembly inspection must confirm.

Do not remove thermal vias just to make the solder process easier. Compare the via treatment and stencil pattern against the package guidance, electrical connection, thermal target and fabrication capability, then verify the assembled joint on representative hardware.
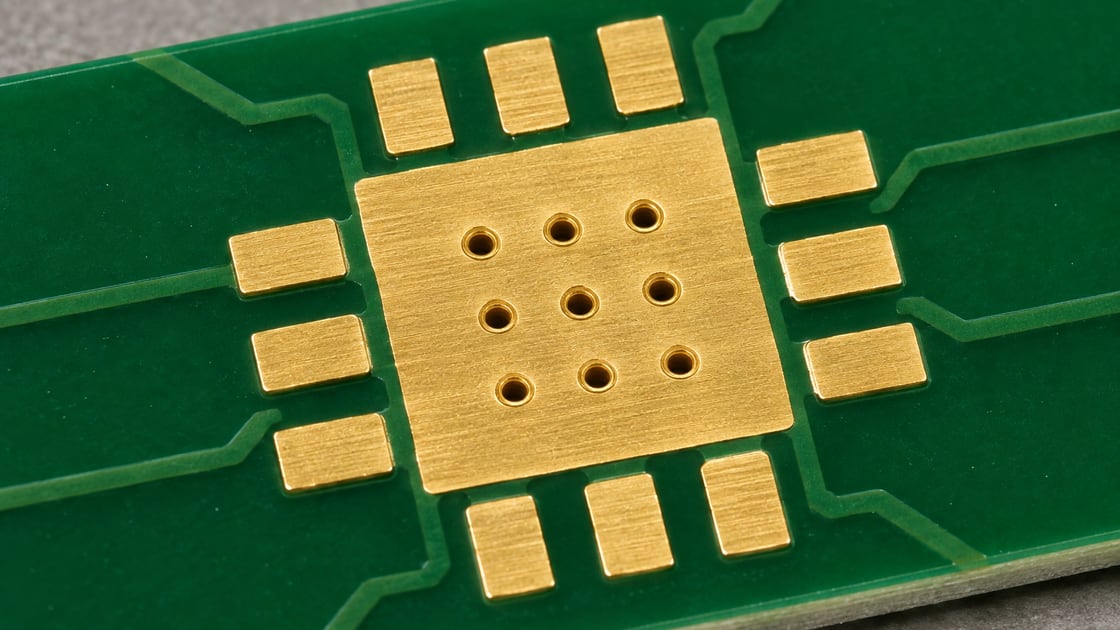
Unpopulated PCB land with several plated via openings
Via positions under a stencil aperture change how exposed openings interact with the paste. AI-generated illustration; not a production or test record.

thermal via solder wicking

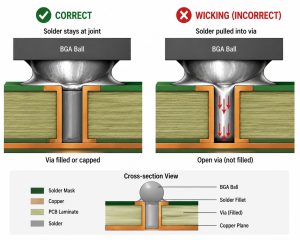
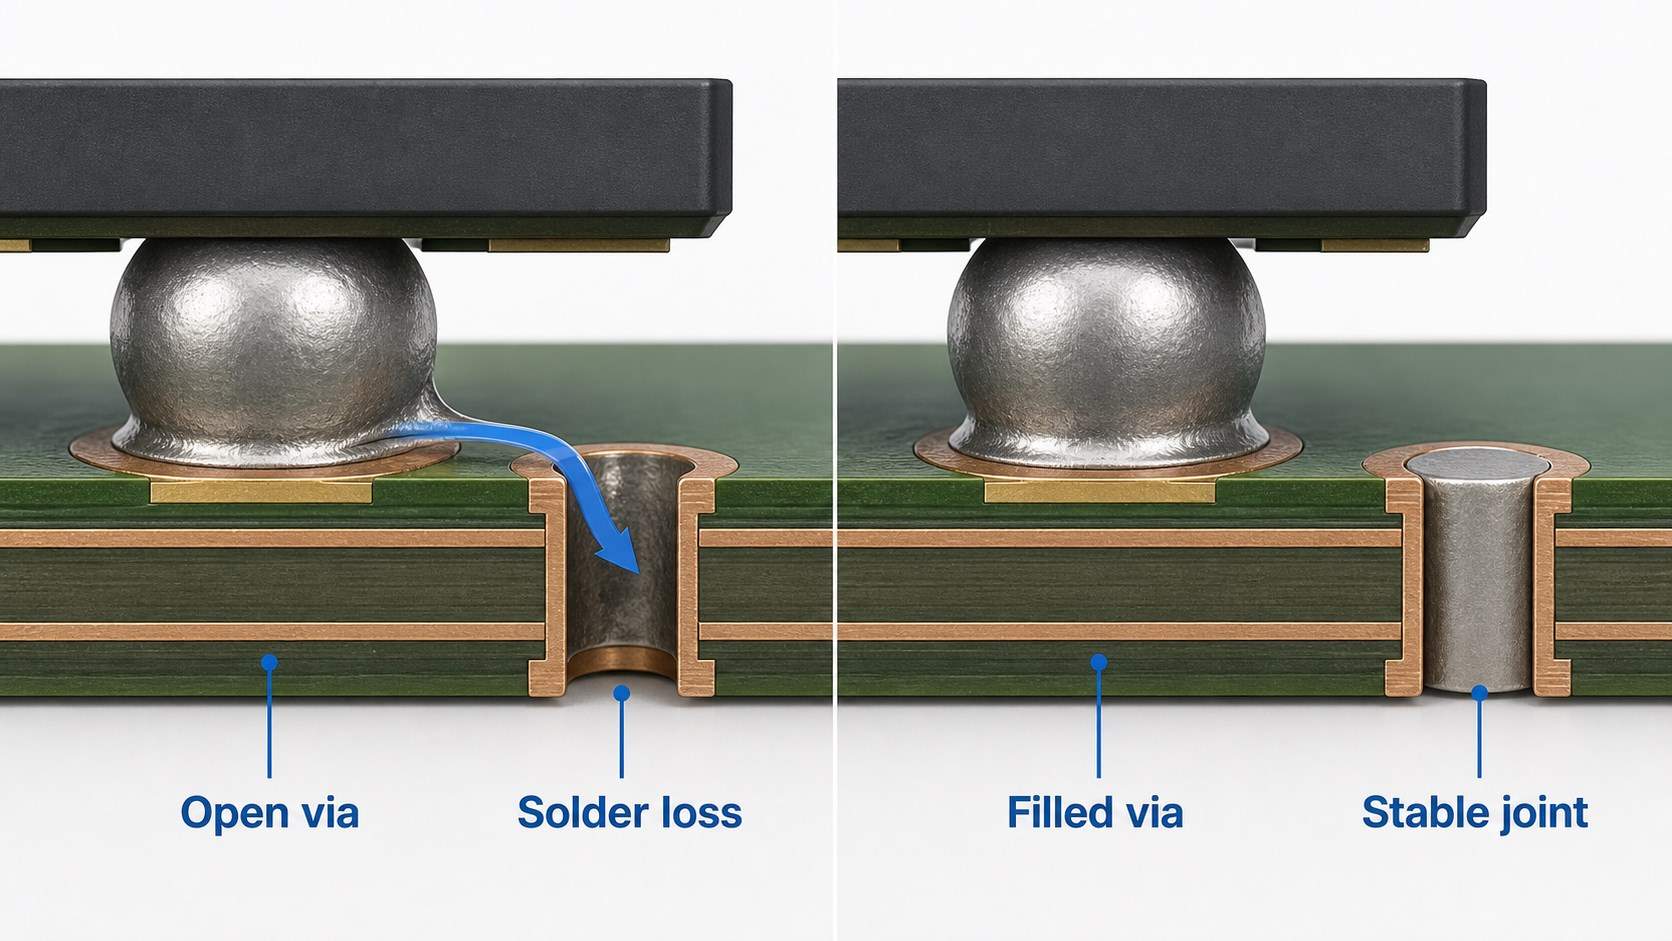
An open, wettable via inside the pasted land creates a path for solder during reflow. The amount that enters depends on the opening, plating and wetting, available solder and process conditions. It is not enough to count vias or compute their empty volume. TI’s PowerPAD application report discusses controlling hole size and stencil placement for the packages it covers.

Check the actual joint for loss of solder and the reverse side for protrusion or deposits. Do not label every exposed-pad void as wicking; outgassing and paste or reflow behavior can also contribute.

thermal pad via design

Design the thermal and assembly paths as one set of requirements. The exposed pad may have an electrical connection as well as a thermal role; check its required net in the device datasheet. Draw the via array, finished hole openings, paste windows and mask openings on the same coordinate basis so both suppliers can review them.

Parameter Specify or verify
Finished hole Diameter and location
Via treatment Open, tented or capped
Paste windows Size and alignment
Thermal path Net, planes and copper
Evidence X-ray and thermal check

thermal vias size and spacing

Use the exact package recommendation and fabricator capability, not a universal hole diameter or pitch. Smaller openings may limit the solder available to flow into a barrel, but hole size, plating and pitch also affect the heat path and manufacturing yield. In a solder-risk review, ask where each opening lands relative to the stencil windows and what registration margin remains.

The thermal via design overview covers the separate heat-flow and resistance question. This article focuses on deciding which openings can safely remain beneath the soldered land.

should thermal vias be tented

Tenting is an option only if the selected side and mask process are suitable for the package and assembly route. A mask film spanning an opening is not a metal cap. Top-side tenting can affect the wettable pad area; reverse-side tenting leaves a top-side opening unless the stack or process specifies otherwise.

Ask whether the supplier can maintain the requested tent through fabrication and reflow at the finished hole size. Compare this with paste windows that avoid open vias, rather than treating tenting as a universal remedy.

thermal via filling

Specify what ā€œfilledā€ means before comparing quotes. A resin-filled via with a metal cap presents a different top surface from an open plated hole; a tented or merely plugged hole is not automatically planar or capped. A nonconductive fill does not remove the existing plated copper path, but it should not be modeled as a solid copper cylinder.

Option Top surface Check before release
Open plated via Opening exposed Paste clearance
Mask tent Mask film, if intact Side and coverage
Filled and capped Plated surface Flatness and cap integrity
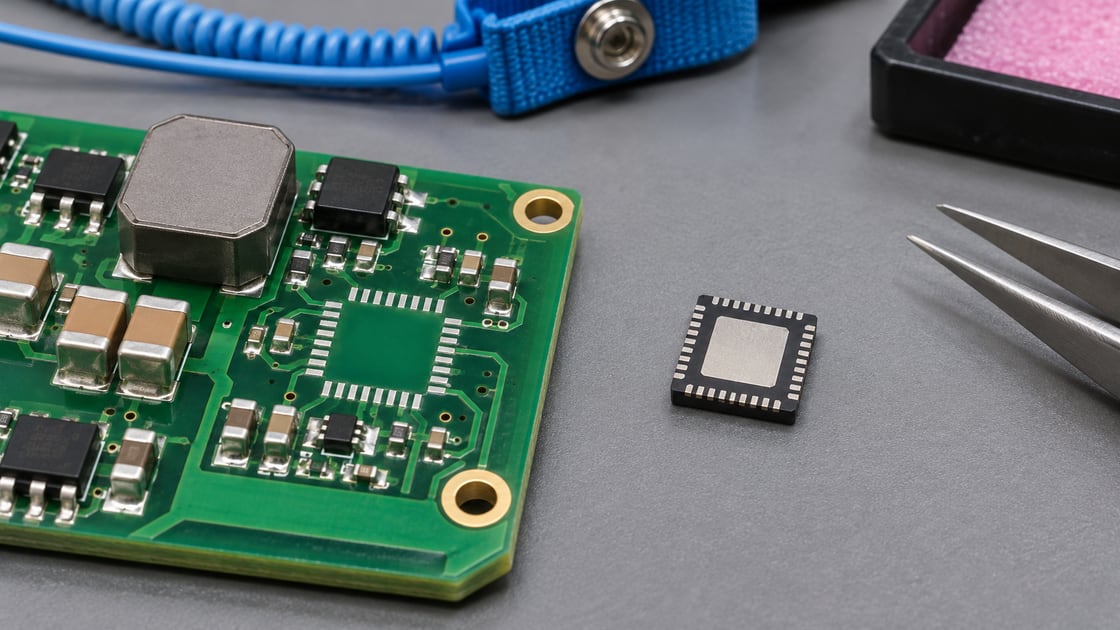
QFN-style component underside and a power PCB sample
Use the exact package drawing when setting the land and stencil geometry. AI-generated illustration; not a production or test record.

via in pad plated over

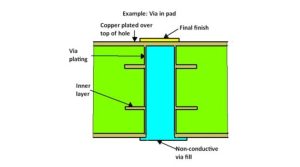
Filled and plated-over via-in-pad can be useful when an uninterrupted solderable land is needed. Confirm the fill, cap plating, finished planarity and inspection evidence rather than approving a quote based only on ā€œVIPPO.ā€ See the via-in-pad plated-over process guide for manufacturing details.

Compare the extra process requirements with an open-hole approach that positions stencil windows away from the vias. Both options need assembly verification. Capping addresses the open-hole path but does not remove every possible cause of voiding.

qfn ground pad stencil design

Segmenting the paste area can help the assembler control deposit distribution and avoid some open holes. Use the package and assembly process recommendations; the stencil thickness and pattern must also suit the peripheral joints. TI’s QFN and SON attachment guidance discusses exposed-pad stencil options and X-ray evaluation.

For a drawing check only, four 1.2 mm square windows on a 3.0 mm square exposed land occupy 5.76 mm² of the 9.00 mm² land, or 64% area. With a 0.10 mm stencil, their theoretical aperture volume is 0.576 mm³. Neither value is a recommended target or a prediction of deposited solder; transfer efficiency and reflow change the result. Inspect the actual printed pattern before treating the layout as qualified.

qfn solder void

Look at the void pattern, remaining joint coverage and any solder on the reverse side together. A two-dimensional X-ray can help locate voids, but it does not by itself prove how a void formed or how much solder entered a specific via. Compare the image with the via locations, stencil layout and process records.

Before approving the design, agree the package-specific acceptance criteria with the assembly team. If the cause is still unclear, choose targeted cross-sections or another agreed inspection. Check the assembled board’s temperature under representative power and ambient conditions; a neat-looking X-ray is not a thermal qualification.

FAQ

Does every open thermal via wick solder?

No. The via and land must interact with molten solder under the actual process conditions. The risk depends on wetting, hole geometry, paste placement and reflow. Inspect both sides of representative assemblies and check the joint before treating a given arrangement as safe.

Is tenting on the bottom the same as a filled and capped via?

No. A mask tent can cover one opening but does not create a plated, planar top land. A filled and capped via uses a different fabrication sequence. Ask for the treatment and inspection details in the fabrication drawing instead of relying on an abbreviated label.

Can I simply reduce the amount of paste to stop wicking?

Reducing paste everywhere can leave an insufficient joint even if less solder travels down the hole. First review where paste overlaps the openings and what the package guidance calls for. Use measured paste deposits and assembled-joint evidence rather than adjusting total paste area alone.

Why are there solder deposits on the opposite side of the board?

An open via connected to the land can be a route for solder during reflow, but other solder processes can also leave deposits. Correlate their locations with the via map and record the assembly sequence. Inspect the top joint rather than assuming the reverse deposit is harmless.

Can a large void prove the exposed pad is not soldered?

A single X-ray view can show a projected void, not the full thickness or shape of a joint. Compare the image with the agreed criteria and inspect the location relative to the pad and vias. Use a suitable follow-up method if the diagnosis affects acceptance.

Will resin-filled vias provide the same thermal result as copper-filled vias?

Do not assume that they will. The barrel, fill, cap and connected planes contribute differently to heat flow. Use the actual cross-section and material properties in a thermal model, then confirm the assembled board when the temperature margin is small.

What must I tell the fabricator before selecting a via treatment?

Provide the package drawing, exposed land and via locations, finished hole sizes, affected sides and required surface condition. Also identify which features must be inspected and whether the assembler expects a flat solderable land. Get the treatment description accepted before releasing the files.

Should I compare a modified stencil using the same assembly process?

Yes, when practical. Keep the package, board, paste and reflow conditions comparable so changes are attributable to the stencil trial. Record print results, joint images and thermal checks together. If several inputs change at once, do not attribute the result to one adjustment alone.

Discuss Your Project

Send Best Technology the device drawing, pad and via layout, finished hole sizes and preferred treatment. Include the stencil and inspection requirements if they are already agreed. Contact sales@bestpcbs.com.
You may also like

What Is Solder Wicking in PCB Assembly? Causes and Prevention
Wednesday, July 22nd, 2026

What Is Solder Wicking in PCB Assembly? Solder wicking in PCB assembly is the unwanted movement of molten solder away from the intended solder joint. It usually happens because of capillary action, heat imbalance, open vias, exposed copper, improper solder paste volume, or unsuitable reflow conditions. When solder leaves the pad, the result may be a weak joint, dry joint, insufficient solder, open connection, or long-term reliability risk.

For EBest Circuit (Best Technology), solder wicking is not only a soldering term. It is a real PCBA quality issue that may appear in PCB SMT assembly, through-hole soldering, BGA assembly, via-in-pad structures, connector areas, and rework. If your PCB assembly project has solder joint, BGA, via-in-pad, SMT, stencil, reflow, or inspection concerns, please feel free to send your Gerber files, BOM, assembly drawing, PCB stackup, or soldering notes to sales@bestpcbs.com. Our engineering team can review the manufacturing path before production starts.

what is solder wicking

What Is Solder Wicking in PCB Assembly?

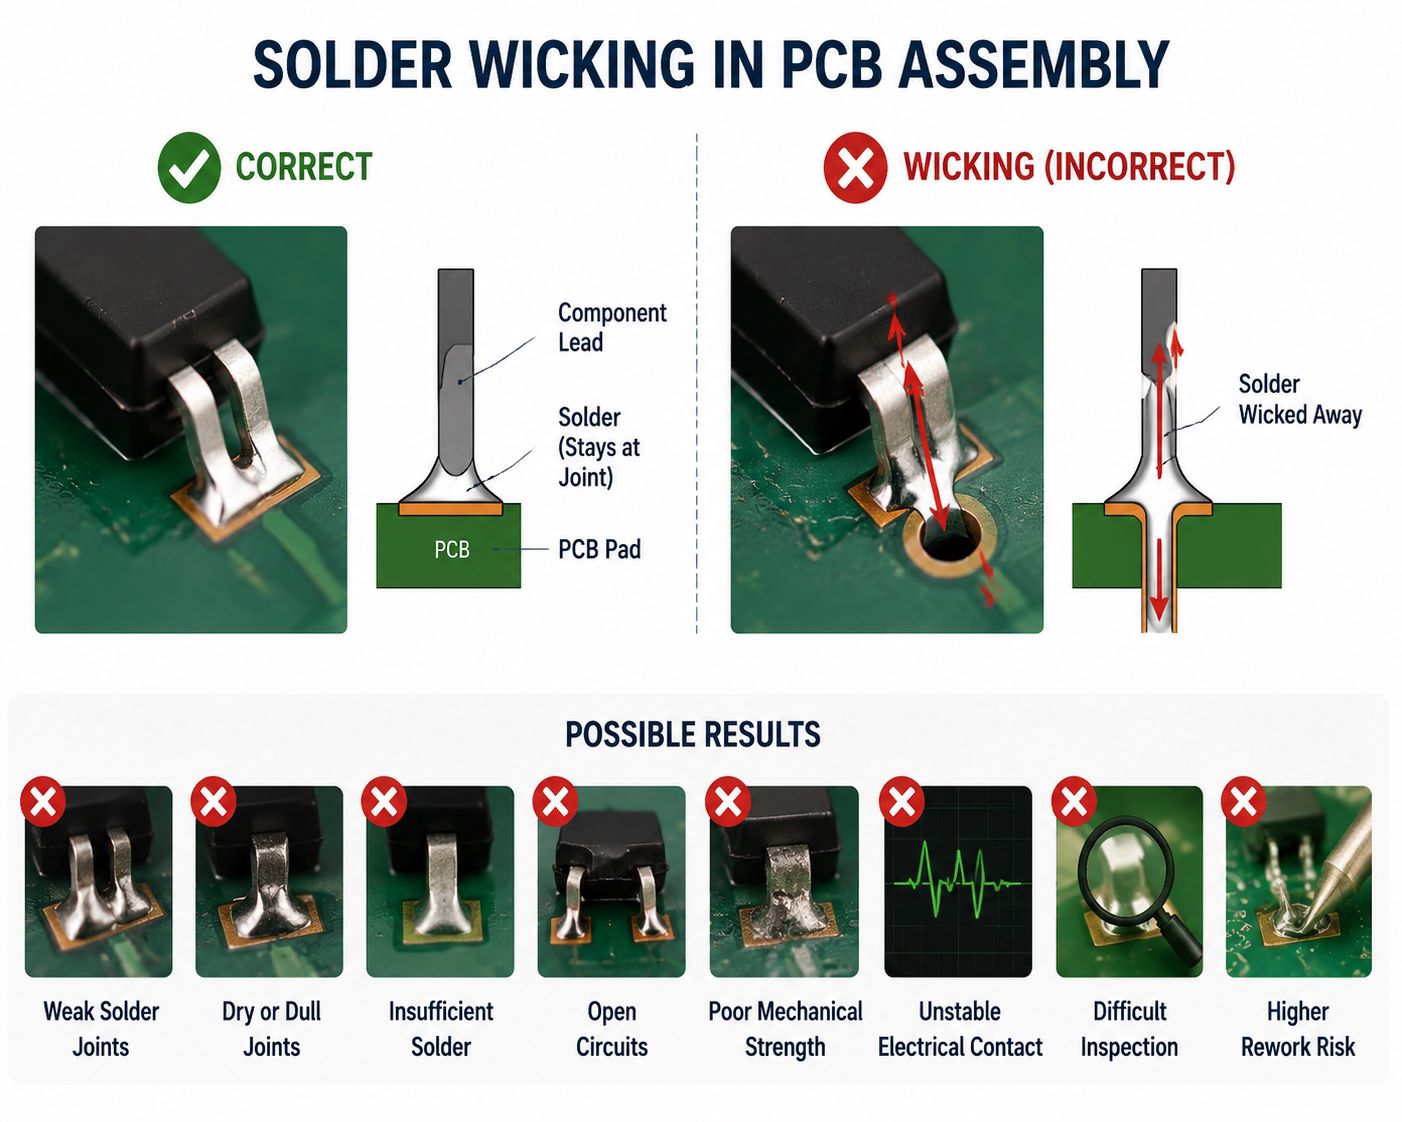
What is solder wicking? Solder wicking means molten solder is pulled away from the place where it should form a joint.

In PCB assembly, solder should stay between the component terminal and the PCB pad. If it flows into a via, up a component lead, along exposed copper, or into stranded wire, the solder volume left at the joint may become insufficient.

Common results include:

  • weak solder joints
  • dry or dull solder joints
  • insufficient solder on pads
  • open circuits
  • poor mechanical strength
  • unstable electrical contact
  • difficult inspection results
  • higher rework risk

Solder wicking is especially important in high-density PCBA projects because small pads, fine-pitch components, via-in-pad designs, BGA areas, connectors, and compact layouts leave less process margin.

what is solder wicking

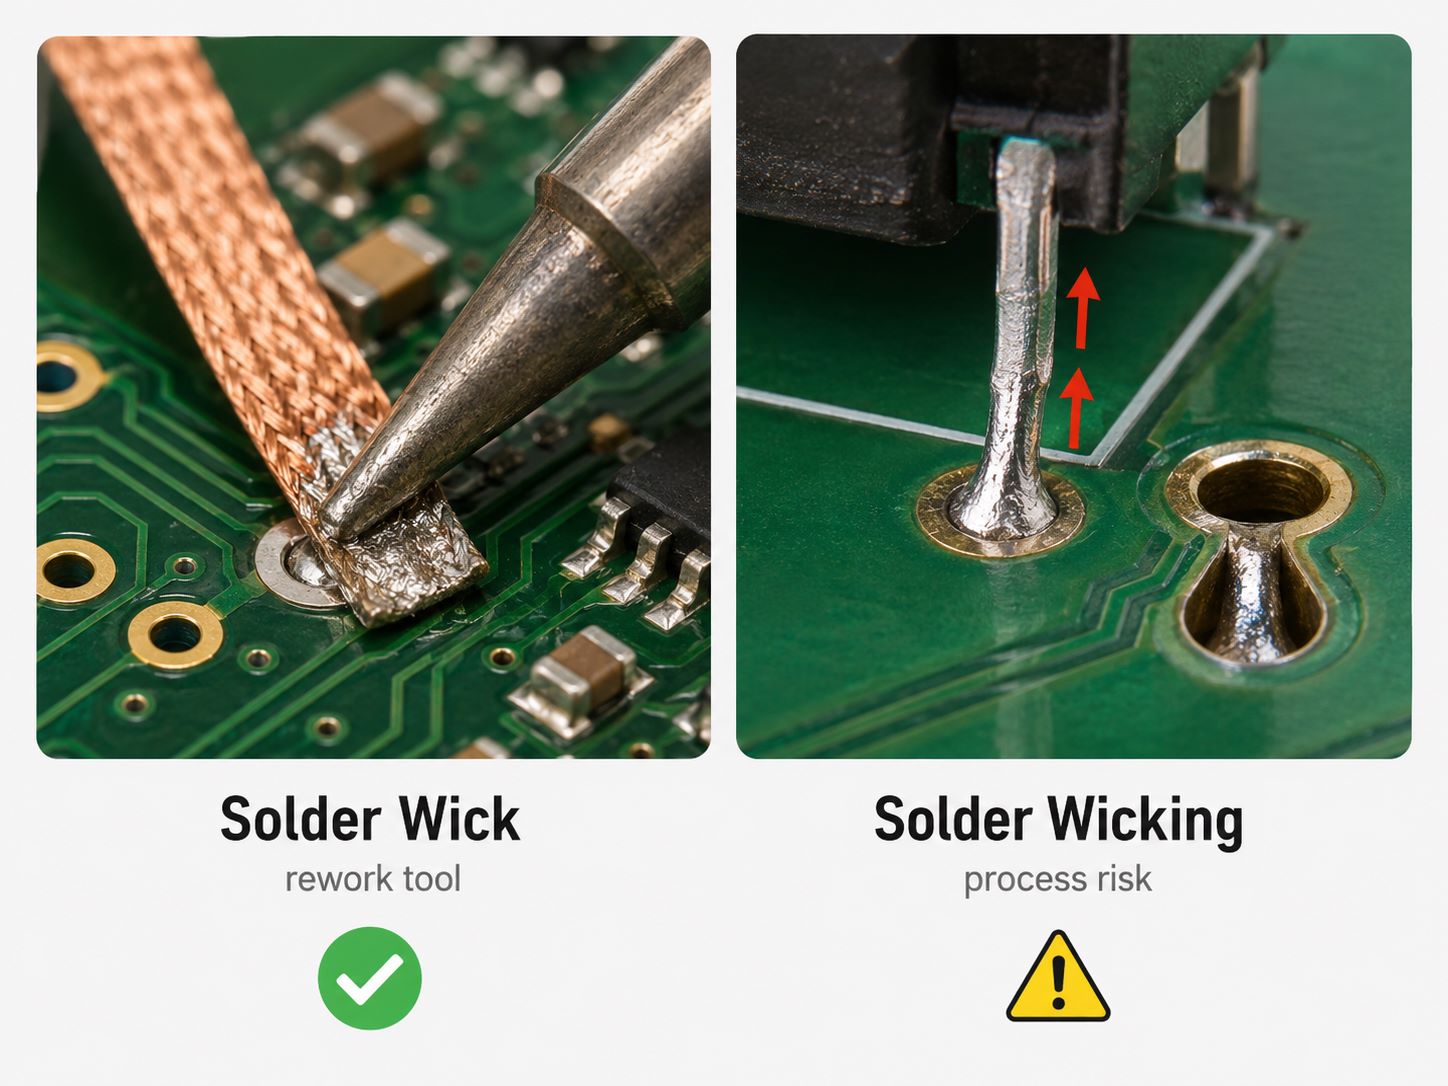
Solder Wick vs Solder Wicking

Solder wick and solder wicking sound similar, but they are not the same thing.

TermMeaning
Solder wickA desoldering braid used to remove solder
Solder wickingA solder flow defect or process risk
Desoldering wickAnother name for solder wick
Wicking solderSolder being pulled away by capillary action

A solder wick is usually a braided copper strip with flux. It is used during rework or repair to remove extra solder from pads, bridges, or component leads.

Solder wicking, however, is usually unwanted. It means solder has moved away from the joint during soldering, reflow, wave soldering, hand soldering, or repair.

For PCB assembly projects, this distinction matters because the solution is different. Solder wick is a rework tool used to remove solder, while solder wicking is a process risk that should be prevented through PCB layout review, via control, solder mask design, stencil planning, and assembly inspection.

what is solder wicking

What Is Solder Wick Used For?

Solder wick is used to remove solder from a PCB during repair, prototype adjustment, or rework.

It is often used for:

  • removing solder bridges
  • cleaning pads before replacing components
  • correcting excess solder
  • removing solder from through-hole pads
  • preparing pads for reassembly
  • repairing prototype boards
  • cleaning fine-pitch IC pads carefully

The basic working principle is simple. The heated solder melts, and the braided copper wick pulls the solder into itself through capillary action. Flux helps improve wetting and solder flow.

However, solder wick should be used carefully. Too much heat, too much pressure, or long contact time can damage pads, solder mask, copper traces, or nearby components. If rework is needed on a prototype or assembled PCB, the process should follow a controlled method for how to use solder wick and should be inspected after repair.

What Causes Solder Wicking on PCB Assemblies?

Solder wicking usually has more than one cause. It may come from PCB layout details, fabrication choices, assembly process settings, or repair conditions.

CauseWhat Happens
Open via near padSolder flows into the via
Via-in-pad not filledSolder drains away from the component pad
Exposed copper pathSolder spreads beyond the joint
No solder mask damSolder moves toward nearby copper
Too much heatSolder becomes too fluid
Long heating timeSolder keeps flowing before solidifying
Wrong paste volumeJoint receives too little or too much solder
Poor pad designSolder balance becomes unstable
Wire strandsSolder climbs into the wire
Rework errorExcessive heat pulls solder away

The core issue is usually capillary action. Molten solder is pulled into narrow spaces such as vias, gaps, copper braid, wire strands, or plated holes. If the PCB design or assembly process gives solder an easier path than the intended joint, wicking becomes more likely.

Solder Wicking in Via-in-Pad and BGA Assembly

Solder wicking is a serious concern in via-in-pad and BGA assembly.

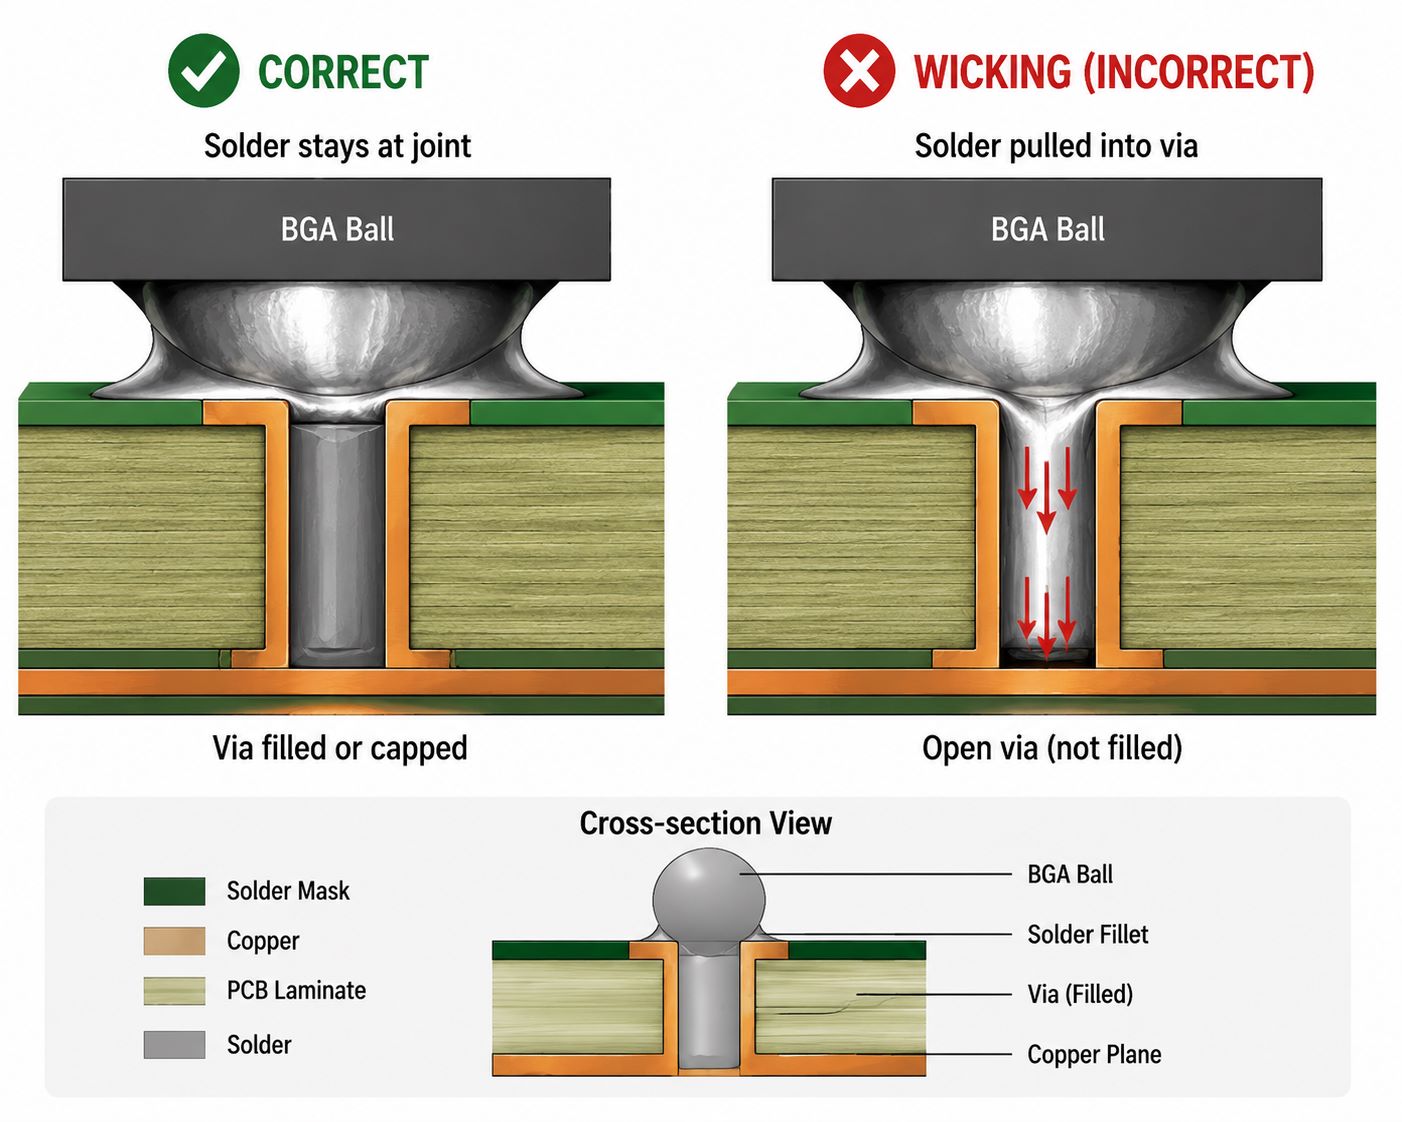
In a BGA area, vias may be placed inside or near pads to support dense routing. If those vias are open, solder can flow into the via during reflow. This may leave too little solder between the BGA ball and the pad.

what is solder wicking

Possible problems include:

  • weak BGA joints
  • insufficient solder volume
  • hidden opens
  • poor coplanarity after reflow
  • unreliable thermal cycling performance
  • difficult X-Ray judgment

For via-in-pad designs, common manufacturing controls include resin-filled vias, plated-over vias, planarization, solder mask control, and proper pad definition. These points should be confirmed before PCB fabrication, not after SMT assembly.

For BGA-related projects, EBest Circuit can review whether the PCB fabrication process, via treatment, surface finish, solder mask opening, and assembly notes match the customer’s production requirements.

You may also refer to our guide on BGA soldering when reviewing BGA assembly risks.

what is solder wicking

Solder Wicking in Through-Hole Components and Wires

Solder wicking can also happen in through-hole components and wires.

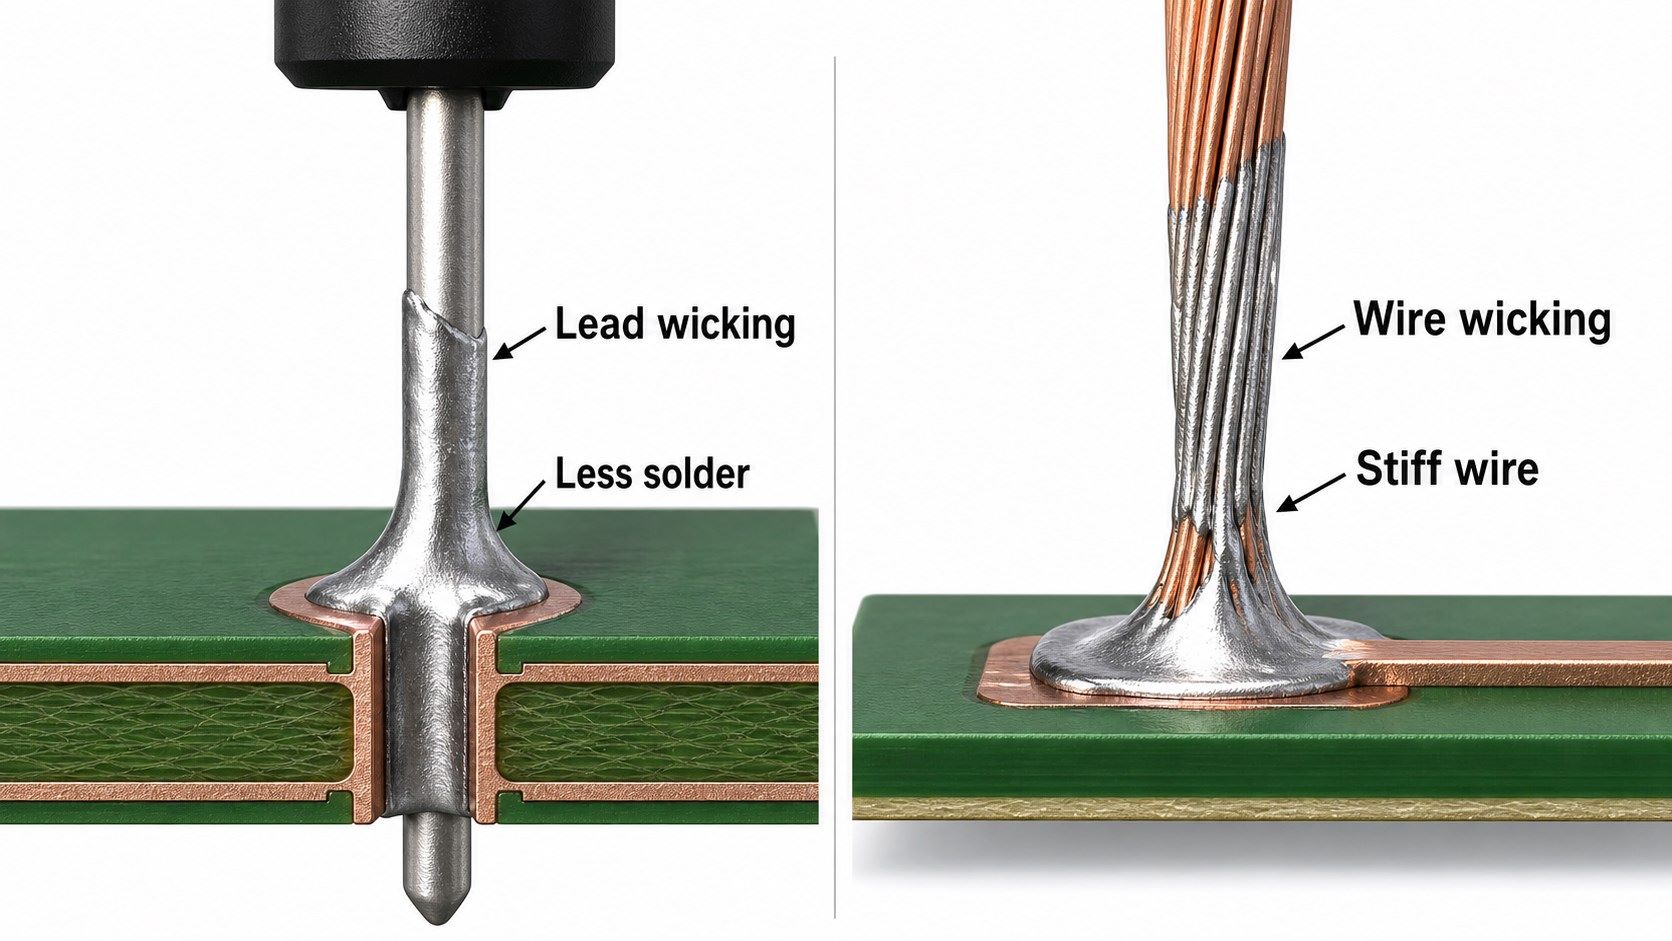
For through-hole components, solder may climb up the lead instead of staying around the plated through hole and pad. This can happen when the lead, hole size, heating time, flux activity, and solder volume are not balanced.

For stranded wires, solder can travel up the wire strands. A small amount of solder flow may be acceptable in some cases, but too much wicking can make the wire stiff. This may create mechanical stress near the solder joint, especially when the wire bends during use.

Areas that need attention include:

  • connectors
  • terminal blocks
  • wire-to-board joints
  • power input areas
  • hand-soldered components
  • reworked pads
  • cable assemblies
  • high-vibration applications

For PCBA projects with wires or through-hole parts, the assembly notes should clearly define soldering requirements, acceptable solder height, cleaning needs, inspection standard, and packing method.

what is solder wicking

How to Prevent Solder Wicking During SMT Assembly

Solder wicking prevention should start before production.

Useful checks include:

  • keep vias away from pads when possible
  • use filled and capped vias for via-in-pad
  • maintain enough solder mask dam between pads and vias
  • confirm pad size and solder mask opening
  • review stencil aperture design
  • control solder paste volume
  • check reflow profile
  • avoid excessive heating during rework
  • inspect solder paste printing with SPI
  • inspect finished solder joints with AOI or X-Ray when needed

For SMT assembly, the solder paste process is especially important. If paste volume is too low, the joint may be weak. If paste volume is too high, solder may bridge or flow into unwanted areas. The correct stencil design depends on pad size, component type, pitch, paste type, board finish, and assembly risk.

Reflow temperature also matters. A profile that is too aggressive may increase solder flow problems. A profile that is too weak may cause poor wetting. The right profile should match the solder paste, component thermal mass, PCB thickness, copper distribution, and assembly complexity.

You may also find our guide on solder temperature for PCB useful when reviewing soldering process conditions.

How to Inspect and Repair Solder Wicking Defects

Solder wicking defects should be checked at the right process stage.

Inspection methods may include:

  • visual inspection
  • SPI after solder paste printing
  • AOI after reflow
  • X-Ray for BGA, QFN, and hidden joints
  • electrical testing
  • functional testing
  • microscope inspection for rework areas

A solder wicking defect may not always be obvious from the surface. In BGA or via-in-pad assembly, the problem may be hidden under the component. That is why X-Ray inspection is important for selected high-risk packages.

Repair depends on the defect type. Some joints can be corrected by controlled rework. Some BGA or via-in-pad issues may require component removal and reballing or replacement. If the root cause is open via-in-pad design or insufficient via filling, repair alone may not solve the problem for future batches.

A good repair process should answer three questions:

  • Is the solder joint electrically reliable?
  • Is the solder joint mechanically reliable?
  • Has the root cause been corrected before the next build?

EBest Circuit PCBA Quality Control for Solder Wicking Risks

EBest Circuit controls solder wicking risks as part of the full PCB and PCBA manufacturing process.

Our support includes:

  • DFM review before production
  • PCB fabrication process review
  • via-in-pad and resin-filled via review
  • solder mask opening check
  • BOM and assembly file review
  • SMT process planning
  • solder paste printing control
  • SPI, AOI, and X-Ray support when required
  • through-hole and hand soldering process control
  • rework and inspection support
  • prototype and small-batch production

This is important because solder wicking is not only an operator issue. It may come from the PCB structure, via design, pad design, solder mask, stencil, paste volume, reflow profile, component type, or rework method.

EBest Circuit provides one-stop PCB fabrication, component sourcing, PCBA assembly, testing coordination, and engineering review. For projects with BGA, fine-pitch ICs, via-in-pad, connectors, wire soldering, or high-reliability requirements, this integrated workflow helps keep manufacturing details visible from file review to final delivery.

FAQs about Solder Wicking and Solder Wick

1. What is solder wicking?
Solder wicking is the unwanted movement of molten solder away from the intended solder joint. In PCB assembly, it may cause insufficient solder, weak joints, dry joints, or open connections.

2. Is solder wick the same as solder wicking?
No. Solder wick is a desoldering braid used to remove solder. Solder wicking is a solder flow problem or defect where solder is pulled away from the joint.

3. What is solder wick used for?
Solder wick is used for removing solder bridges, cleaning pads, repairing prototype boards, and preparing pads for component replacement during rework.

4. How do you prevent solder wicking in PCB assembly?
Prevention methods include proper via placement, filled via-in-pad, solder mask dams, correct stencil aperture, controlled solder paste volume, suitable reflow profile, and inspection after SMT.

5. Why is solder wicking a problem in BGA assembly?
In BGA assembly, solder wicking may pull solder into open vias or away from pads. This can create weak or hidden solder joints that may require X-Ray inspection.

In summary, if your PCB or PCBA project involves BGA assembly, via-in-pad, fine-pitch SMT, through-hole soldering, connector soldering, rework, or solder joint quality concerns, please feel free to contact sales@bestpcbs.com. EBest Circuit’s engineering team can help review your files and manufacturing notes before production, so soldering risks are addressed earlier instead of discovered after assembly.
You may also like