A laminated busbar lowers inductance when the outgoing and return currents follow closely spaced, overlapping copper plates. It helps less if the current must separate at the capacitor terminals, mounting tabs or switching module. Before choosing a laminated busbar over a heavy copper PCB, trace the complete switching current loop and compare the inductance of the assembled paths, not just the copper weight or the busbar by itself.
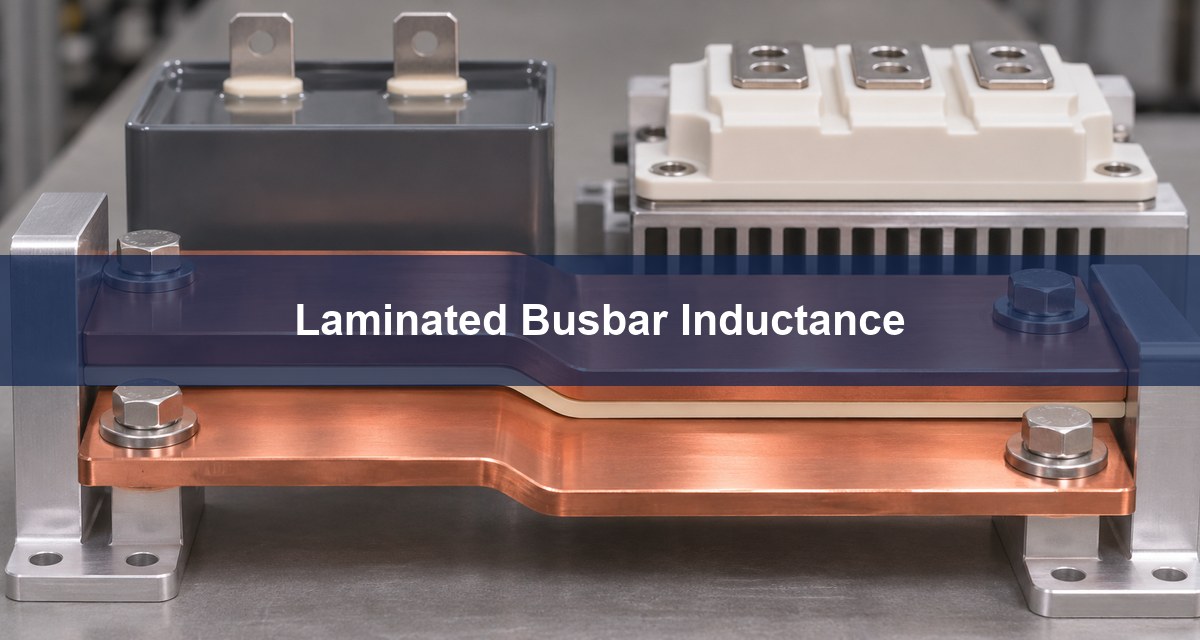
Illustrative unpowered busbar assembly; not a tested product or a verified installation.
Laminated busbar inductance
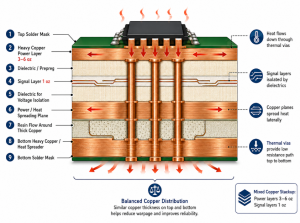
Inductance describes the voltage associated with changing current. In a laminated pair, close parallel plates carrying equal currents in opposite directions confine much of the magnetic field between them. The loop usually has less inductance than two conductors routed far apart. Thick copper lowers DC resistance, but it does not by itself bring the return path closer. In a heavy copper PCB, closely spaced power and return planes can use the same principle.
Keep two numbers separate: the inductance between the busbar’s defined terminals and the effective inductance of the assembled switching loop. A low first number does not guarantee a low second one. Infineon’s PrimePACK application note shows how a laminated DC-link connection is arranged at a module.
DC link busbar
The DC-link busbar connects the DC source and capacitor network to the switches. The path carrying average supply current need not be the path carrying the fastest current change. For a half-bridge, trace the loop from the effective local DC-link capacitor through the switch positions and back to the opposite capacitor terminal. Include the capacitor’s terminal and internal inductance, the busbar or board conductors, the joints and the module package. Clearly identify which external paths are outside this loop.
For example, an inverter layout may have a long DC feed and a short, well-coupled path to the nearest film capacitor. Shortening the feed does not necessarily fix switching overshoot. Conversely, moving a capacitor closer by straight-line distance may not help if its terminal geometry forces the positive and negative connections apart.
Commutation loop inductance
As a first-pass estimate, the inductive voltage contribution is L × |di/dt|. If the design allocates 40 V to this contribution and the applicable current slope is 4 A/ns, the effective loop budget is 10 nH. This is an illustrative allocation, not a device limit. An estimated 15 nH at the same slope contributes approximately 60 V. Do not add that number directly to a measured peak as if ringing, device capacitance and observation point did not matter.
The useful quantity belongs to a defined loop under the conditions of interest. Changes in current distribution and mutual coupling can make a schematic sum of isolated conductor values misleading. The published study on SiC converter busbar design separates the busbar, capacitor, connector and package contributions and shows why the terminals belong in the analysis.
DC link capacitor busbar
Review both capacitor terminals with the return route visible. A large remote capacitor bank can support stored energy and slower ripple while a nearby low-inductance path supplies fast switching current. Parallel capacitors do not automatically share high-frequency current equally: different placement, terminations and parasitic inductances change the current distribution. A short broad path is only helpful if it remains paired with its return close to the capacitor and at the module.
In the inverter example, if the positive tab is on the near edge and the negative tab returns around a mechanical opening, the loop can be dominated by that opening rather than by the flat overlap. Ask for the assembled geometry and compare alternative terminal orientations before paying for a thicker pair of plates.
Laminated busbar design guide
Choose a laminated assembly when separate formed conductors better meet current, mechanical or terminal constraints. Choose a heavy copper PCB when closely paired layers meet the same loop budget and integration is more important. Use separate conductors only when the fast switching loop is controlled elsewhere or when measured inductance still meets the requirement.
Laminated busbar vs. heavy copper PCB vs. separate bars
Construction
When it fits
What to verify
Laminated busbar
Broad paired conductors are possible, with heavy terminal loads.
Plate overlap at the tabs, assembly alignment and the insulation system.
Heavy copper PCB
A layered return path and integrated routing fit on one board.
Layer spacing, via and terminal transitions, current distribution and temperature rise.
Separate bars
The conductors carry feed current and a separate compact path closes the fast loop.
The location of the actual switching loop and measured switching stress.
A busbar’s dielectric spacing cannot be chosen from inductance alone. For products where IEC 60664-1 applies, coordinate the insulation design with the responsible compliance engineer and the applicable product standard. Close spacing does not waive separate checks at exposed edges, cutouts and terminals.
Busbar inductance calculator
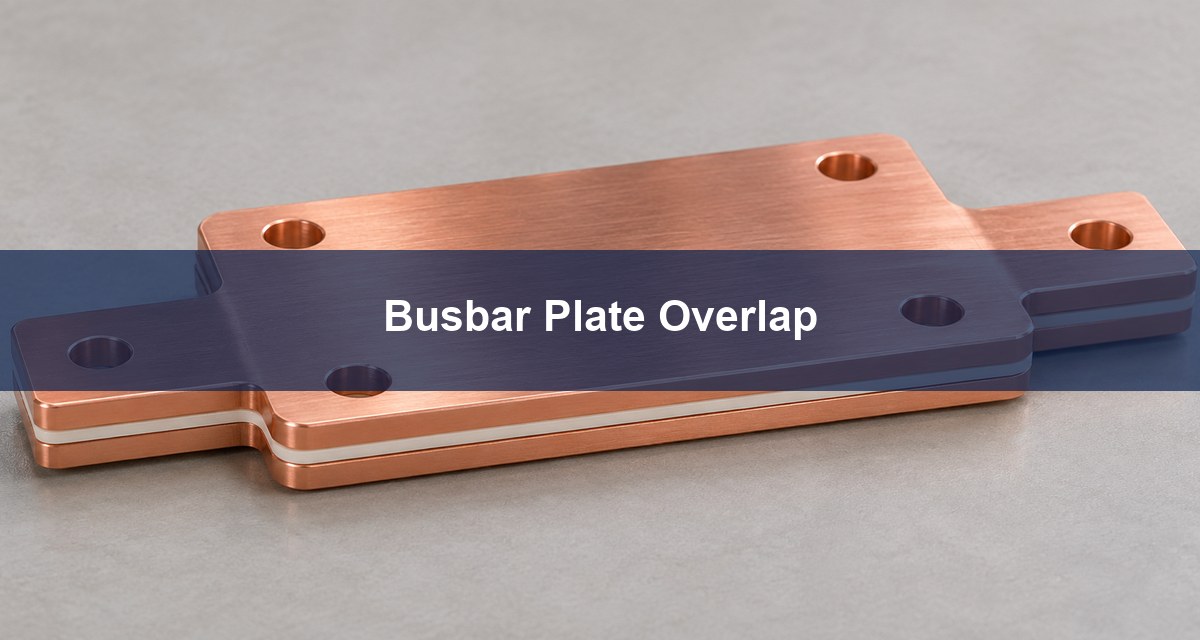
Use a parallel-plate estimate only to compare the straight, broad overlap regions with the same assumptions. In its wide-plate limit the estimate is μ₀ times overlap length times plate separation divided by width, for a nonmagnetic spacer. For a 100 mm long overlap, 50 mm wide, with 0.50 mm separation, this gives about 1.26 nH. Doubling separation gives about 2.51 nH with the other inputs unchanged. These are idealized straight-section estimates, not assembled loop values or measured data.
The estimate assumes closely spaced plates, approximately opposing currents and width much greater than separation. It omits end effects, joints, apertures and curved tabs, and does not predict current crowding or resonant impedance. Use field extraction or a supplier model with the actual geometry and frequency band if a transition can dominate. Record the port pair on every result so that two nominally identical values are comparable.
Illustrative plates and spacer. The visible overlap does not include the complete current path.
Laminated busbar manufacturing process
Manufacturing must reproduce the conductor spacing and alignment used in the electrical review. Do not approve a busbar from a front-view drawing alone. Specify the plate stack, terminal datums, allowed misalignment and the insulating construction at holes, edges and bends. A nominal spacing that looks favorable in a field model is not enough if the assembled tabs must splay apart to reach the module.
For the related heavy copper board, define the board stackup and joint geometry that form the same current path. The Best Technology busbar PCB design article covers broader board integration. The product drawing and contract should identify the applicable board performance requirements, for example IPC-6012 for qualifying a rigid board where specified; that does not qualify the separate busbar insulation or the assembled loop.
Double pulse test waveforms
On a qualified laboratory setup, compare turn-off voltage and current at the same reference points under comparable DC-link voltage, current, device temperature and gate-drive conditions. An apparent improvement can come from a slower current edge, a different measurement loop or probe error. Log the current slope, peak voltage, ringing and exact setup with each trace. A bench switching waveform by itself does not certify insulation, thermal performance or behavior over all operating points.
Verification evidence before design release
Evidence
What it answers
What to hold constant or record
Simplified overlap estimate
How the straight section responds to geometry changes.
Plate length, width and separation; model omissions.
Field extraction or impedance measurement
Whether termination and connection geometry dominate the path.
Port locations, fixture treatment and frequency range.
Switching waveforms
Whether peak stress meets the design budget on a representative assembly.
Switch, gate drive, DC-link voltage, current, temperature and probe reference.
Release the change only after representative switching conditions meet the project’s documented voltage margin. If the model improves but the waveform does not, revisit the capacitor path, the terminal transition and measurement setup before another copper revision.
FAQ
Does thicker copper automatically lower the switching-loop inductance?
No. It can lower resistance, but the proximity and continuity of the opposing current paths drive much of the geometric inductance.
Why can the nearest capacitor still behave as if it is far away?
Its effective path includes both terminals and the complete return. A short positive lead with a long negative return can still produce a large loop.
Can a busbar have low DC resistance and high switching overshoot?
Yes. Voltage drop in steady operation and inductive voltage during fast current change are different measurements.
Is a low supplier inductance number enough to release the assembly?
No. Ask where it was measured and whether it includes the joints, module and capacitor path used in the final assembly.
Can I fix poor geometry by adding more bulk capacitance?
Not necessarily. If the extra capacitor is coupled through the same high-inductance path, it may affect slower ripple more than the switching edge.
Does a tighter laminated stack always help?
It can reduce the straight-section inductance, but an insulation or assembly constraint may set the minimum spacing. The tabs can still dominate.
Is busbar inductance the same as gate-loop inductance?
No. The gate-drive loop is a separate path with its own reference and geometry. Improving the power path does not automatically correct gate ringing.
What belongs in a fabrication review package?
Send the assembly drawing with terminals, board stack, current-loop sketch, any insulation constraints and the switching conditions used for your limit.
Prepare a heavy copper PCB review
Contact Best Technology at sales@bestpcbs.com with your stackup, terminal drawing and current-loop sketch. Identify whether you need a board-based current path or an external busbar interface so the mechanical and board constraints can be reviewed together.
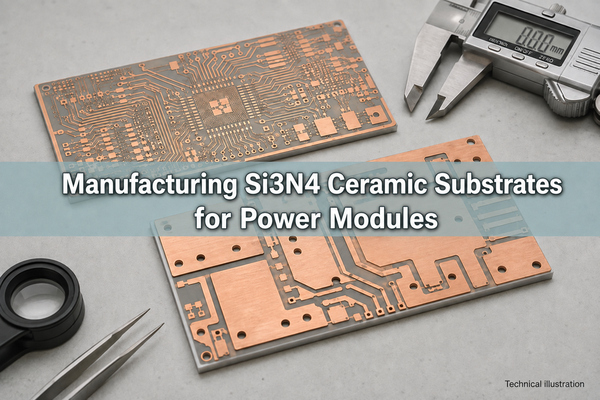
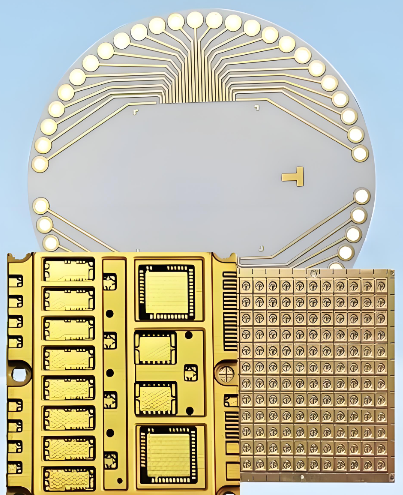
At EBest Circuit (Best Technology), we manufacture Si3N4 ceramic circuit substrates for power electronics using AMB and DPC processes. As a Si3N4 substrate manufacturer, we build the patterned copper structure that connects power devices, transfers heat and maintains electrical isolation. For a power module, the manufacturing challenge is to make that structure work through repeated heating and cooling, not simply to choose a ceramic with a high conductivity number.
The Si3N4 chemical name is silicon nitride. In a silicon nitride ceramic substrate, the ceramic provides insulation while the metal layers form the circuit. Silicon carbide, or SiC, is different: a SiC semiconductor die can be mounted above a silicon nitride substrate, with each material performing a different job.
Why Do Thermally Cycled Power Modules Use Si3N4?
Power devices heat up under load and cool when the load falls. Copper and ceramic expand by different amounts, loading their bonded interface during each cycle. Si3N4 ceramic is attractive here because its resistance to crack propagation can support demanding copper-ceramic designs while retaining electrical insulation and a useful heat path.
This is why we consider the mechanical properties of silicon nitride alongside thermal performance. High silicon nitride thermal conductivity alone does not describe how a metallized substrate responds to copper thickness, edge defects or repeated temperature swings. The following Si3N4 material properties illustrate the different inputs to that decision.
Design input
Electronic-substrate grade example
Question it helps answer
Si3N4 thermal conductivity
85 W/m·K at 25°C
How much thermal resistance does the ceramic thickness add?
How does the selected grade resist crack growth and bending?
Si3N4 thermal expansion coefficient
2.6 ppm/K over 40–400°C
What expansion mismatch must the copper-ceramic structure accommodate?
Si3N4 Young’s modulus
310 GPa
How stiff is the ceramic in the mechanical model?
These are reference values for one commercial grade, not our finished-board acceptance limits. Use the selected grade’s silicon nitride coefficient of thermal expansion over the relevant temperature interval; a room-temperature value cannot describe an entire operating cycle.
Si3N4 properties make the material a strong candidate when mechanical reliability and heat removal must be addressed together. An AlN substrate may still be preferable where reducing ceramic-layer thermal resistance dominates the design, while alumina can suit less demanding, cost-sensitive circuits. The choice should follow the module’s loading and cooling requirements rather than a universal material ranking.
Building the Copper-Ceramic Structure with AMB
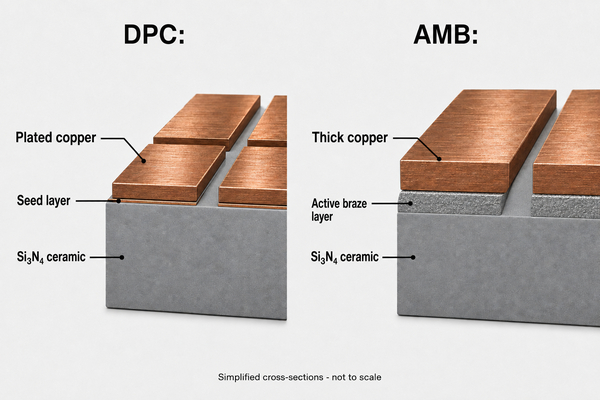
For a thick-copper power circuit, our AMB ceramic PCBs provide a manufacturing route that joins copper to the ceramic through active metal brazing. A Si3N4 AMB substrate combines current-carrying copper regions with an insulating ceramic core; the brazed interface connects the materials mechanically and thermally.
Define the stack. We review the silicon nitride Si3N4 plate, copper on each face, finished dimensions and assembly surfaces against the circuit drawing.
Join copper to ceramic. An active brazing material enables the metal-ceramic bond. This is a metallurgical joining layer, not an adhesive film.
Form the isolated circuit regions. Patterning must define both the copper geometry and the required electrically isolated spaces. Conductive residues between islands cannot remain as unintended current paths.
Finish the connection surfaces. We match the specified finish and pad condition to the subsequent attachment process before the circuit enters module assembly.
The copper thickness and isolation geometry must be developed together. Etching a thick conductor produces a sidewall profile, so the gap visible at the copper surface is not necessarily the same as the metal-free distance at the ceramic interface. We review the finished geometry, not only the artwork line.
Choosing DPC for Finer Si3N4 Circuit Geometry
Not every silicon nitride circuit needs thick brazed copper. If the design requires finer conductor geometry or thinner controlled metallization, our DPC ceramic PCBs offer another route. Direct plated copper uses deposited metallization and copper plating to create patterned tracks and pads on the ceramic.
A smaller feature capability is useful when connection density drives the layout, but it does not make DPC an automatic substitute for an AMB substrate carrying a different current or heat load. We select the route against the conductor structure and attachment requirements before applying the dimensional limits below.
Our Si3N4 Substrate Manufacturing and Customization Capabilities
We manufacture custom Si3N4 ceramic circuits with the copper layout, board outline and connection surfaces specified for the project. The following DPC and AMB process capabilities establish a starting point for engineering review; they are not a promise that every maximum and minimum can be combined on the same board.
Item
Our DPC process
Our AMB process
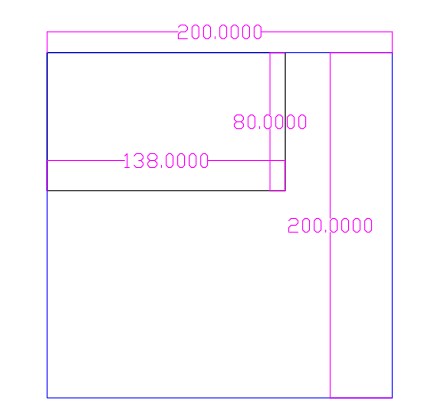
Maximum panel size
138 × 190 mm
114 × 114 mm
Copper thickness
2–200 µm
8–22.9 oz, about 0.28–0.80 mm
Minimum line / space
6 / 8 mil, about 0.15 / 0.20 mm
20 / 20 mil, about 0.50 / 0.50 mm
Circuit layers
Two-layer capability
Two-layer capability
Surface finish options
OSP, ENIG, immersion silver
OSP, ENIG, immersion silver
Customization covers the conductor pattern, pad locations, outline, hole positions and specified finish. We confirm ceramic grade and thickness with the copper construction rather than applying a generic ceramic thickness list to every Si3N4 build. Panel dimensions also include manufacturing margins; they are not the usable circuit area.
Design Details We Review Before Circuit Fabrication
A manufacturable substrate drawing describes more than an outline and a copper thickness. Our custom ceramic PCB manufacturing review connects the circuit artwork to the joining process, mechanical support and electrical isolation requirements.
Drawing or assembly input
Our manufacturing review
Why it matters
Copper islands, line spacing and thickness
Review patterning allowance, pad shape and the required isolation after metal removal
Heavy copper changes achievable geometry; narrow gaps require more than a nominal artwork dimension
Ceramic outline, holes and registration references
Check the mechanical drawing against the copper artwork and assembly datums
The circuit must align with the device placement, terminals and module mounting arrangement
Working voltage, ceramic thickness and conductor separation
Define insulation test conditions and review clearance and creepage with the module design
A material breakdown number is not the assembled module’s working-voltage rating
Material Data Needed Beyond the Copper Drawing
For electrical modeling, Si3N4 permittivity is grade- and frequency-dependent; an electronic-substrate example is 7.8 at 1 MHz. The electrical conductivity of silicon nitride is low in its insulating substrate form, so current should follow the copper rather than pass through the ceramic. Parasitic capacitance across that ceramic still matters in a fast-switching module.
Si3N4 density and Si3N4 hardness serve different manufacturing purposes: a grade example lists 3.22 g/cm³ and 15 GPa Vickers hardness. Density contributes to mass estimates; hardness informs machining considerations. Neither replaces fracture-toughness or edge-quality requirements when assessing a thin circuit plate.
Controlling Warpage and Edge Stress in Thick-Copper Si3N4 Substrates
Warpage control starts with the copper-ceramic construction, not just a flatness check at shipment. Copper on the two faces can differ in thickness, coverage and pattern position. Those differences, together with ceramic thickness and substrate dimensions, affect how the part bends as the bonded structure changes temperature.
During layout review, we examine the relationship between the front and back copper patterns, large copper islands, ceramic borders and assembly support points. Symmetry can help, but forcing identical copper on both faces may conflict with the electrical design. An asymmetric stack needs its own assessment rather than a universal rule that one copper ratio guarantees flatness.
At the perimeter, copper geometry, the metal-free ceramic border and existing edge defects influence local loading. Thick copper should not simply be extended to the ceramic edge to gain conductor area. We agree the relevant clearances and edge-acceptance criteria for the selected stack.
For a demanding mounting interface, the drawing should define the flatness measurement area and support condition. Initial samples can then be checked against the intended attachment surface before the construction is released for production. Substrate bow should not be corrected by forcing a brittle ceramic plate flat with excessive clamping load.
Selecting Surface Finishes for Die Attach and Interconnection
Surface finish selection must follow the assembly method. The same Si3N4 circuit can have die-attachment pads, wire-bond areas and an underside thermal interface, each with different requirements. A coating name alone does not specify a bondable or sinterable surface.
Soldered attachment: match the surface condition to the solder and flux system, storage controls and planned thermal exposures. Oxidation or contamination can undermine wetting even when the nominal finish is correct.
Wire bonding: identify the wire material and bonding process, then specify compatible pad metallurgy, cleanliness and roughness. A finish qualified for soldering is not automatically qualified for wire bonding.
Silver-sintered attachment: where the module design uses this method, confirm the paste’s required substrate and die-backside metallization. An immersion-silver option does not by itself establish a qualified sintering process.
We use the attachment specification to review the circuit’s finish requirements and achievable surface condition. The module assembler must validate the joining process on that surface. This keeps substrate fabrication and assembly qualification connected without implying that every finish or assembly process is interchangeable.
Matching the Substrate to the Module and Cooling Stack
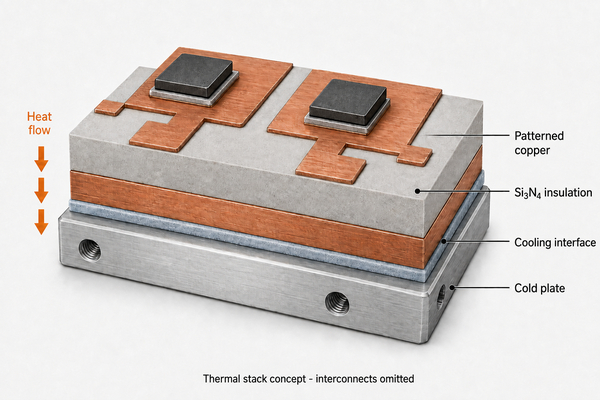
In the finished assembly, heat travels from the semiconductor through its attachment layer, the upper copper, the ceramic and the lower interface toward a baseplate or cooler. The ceramic contributes only one part of that path. For a simplified uniform layer, its thermal resistance is R = t / (k × A), where t is thickness, k is thermal conductivity and A is heat-transfer area.
Traction-Inverter Power Stages
Repeated acceleration and changing load create thermal excursions in the power stage. A Si3N4-based structure can address the combination of copper loading and ceramic crack resistance. For the circuit build, we need the device-pad layout, copper thickness, substrate attachment method and operating temperature range; the module design must also account for interconnect and joint fatigue.
Charger and Industrial-Drive Power Stages
In a charger’s switching bridge or an industrial drive’s power module, sustained losses and switching transients place demands on both heat removal and insulation. Substrate dimensions, conductor separation and the underside mounting surface therefore need to be developed with the cooling and packaging arrangement. Choosing a thinner ceramic solely to reduce thermal resistance can change insulation and mechanical margins.
These are application design scenarios for the circuit substrate, not claims that we manufacture complete traction inverters, chargers or motor drives. The illustration shows the heat-path concept; it is not a customer module or a production photograph.
Circuit Acceptance and Module-Level Validation
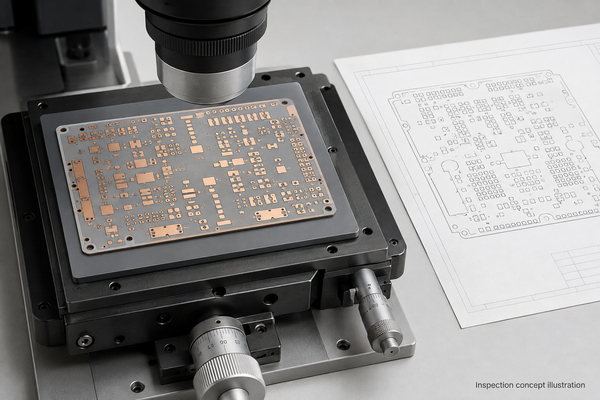
As a silicon nitride substrate manufacturer, we work with you to define acceptance requirements for the fabricated circuit. The inspection plan should address conductor geometry, continuity and isolation, ceramic edge condition, finished dimensions, flatness and surface condition. Joining-interface inspection requirements and suitable methods should be agreed for the selected process.
A circuit inspection and a module qualification answer different questions. The first checks whether the substrate meets its drawing and acceptance criteria. Thermal or power cycling, partial-discharge testing where required, and assembled thermal-performance validation establish behavior under the module’s actual operating conditions. An optical image cannot demonstrate those lifetime results.
When comparing silicon nitride manufacturers, distinguish bare-material specifications from the ability to manufacture the required copper circuit. Our role is ceramic circuit fabrication, with DPC or AMB process selection, manufacturability review and project-specific acceptance planning. We do not describe a raw-material datasheet as our own finished-module performance guarantee.
Si3N4 cost depends on material grade, dimensions, copper structure, finish and quantity. We review these together so the quoted construction matches the drawing. Send your circuit artwork, stack-up, attachment requirements and target quantity to sales@bestpcbs.com; our team can review a manufacturable Si3N4 configuration for your power-electronics project.
An insulated gate bipolar transistor, or IGBT, is a voltage-controlled power switch that combines a MOS gate with a bipolar current path. It is widely used in motor drives, solar inverters, UPS systems, welding equipment and induction-heating power stages because it can control substantial current at high voltage without continuous gate current.
A useful IGBT design starts with more than a part number. You need to decide whether an IGBT suits the converter, read its ratings under the correct test conditions, estimate losses and junction temperature, and then design the gate drive, current loops, cooling and protection as one system. This guide gives you that sequence, with calculations, waveform checks and the information needed for a practical PCB review.
What Is an Insulated Gate Bipolar Transistor?
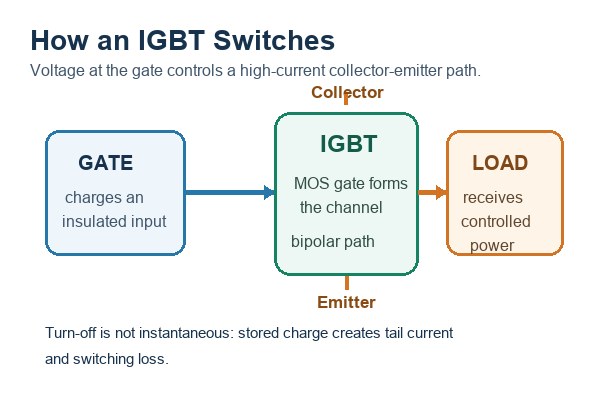
An IGBT is a three-terminal semiconductor used as an electronic power switch. Its gate receives the control signal, while its collector and emitter carry the load current. The insulated input gives the gate high impedance. The bipolar conduction mechanism lowers the on-state voltage in operating regions where high-voltage MOSFET conduction loss may be less attractive.
The three terminals have different jobs. The gate is charged or discharged by the driver. The collector usually connects to the high-voltage side or a switching node. The emitter returns the main current and also provides the voltage reference for the gate drive. Some packages add a Kelvin emitter pin so the driver can avoid voltage error caused by inductance in the power-emitter path.
A discrete IGBT contains one controlled switch. An IGBT module may combine several dies, freewheel diodes, sensors and internal interconnects. Neither is a complete converter. The assembly still needs a DC-link network, isolated or level-shifted gate drivers, current sensing, fault shutdown and a thermal path. This distinction prevents a common mistake: choosing a module by its headline current rating before defining how the system will drive and cool it.
How Does an IGBT Turn Power On and Off?
Gate-emitter voltage creates a MOS channel that enables bipolar conduction from collector to emitter. When the gate is held below its turn-on condition, the device blocks collector-emitter voltage within its rated limits. When the driver raises the gate, the channel forms and permits carrier injection into the drift region. This conductivity modulation supports efficient high-voltage current conduction.
Turning the gate off removes the MOS channel quickly, but charge stored in the drift region cannot disappear instantly. The remaining current decays as a turn-off tail. That tail adds turn-off energy and explains why an IGBT often switches more slowly than a power MOSFET. Higher junction temperature can increase the stored-charge effect, so room-temperature switching results do not establish the worst case.
The driver controls how fast the transition occurs by moving charge through the gate resistance and parasitic inductance. A faster edge may reduce switching duration, but it can increase voltage overshoot, ringing, electromagnetic interference and capacitive turn-on of the opposite switch. The correct target is therefore a controlled waveform with acceptable loss and stress, rather than the shortest possible rise or fall time.
When Is an IGBT a Better Choice Than a MOSFET?
An IGBT is a strong candidate when a converter switches high voltage and substantial current at a moderate switching frequency. A MOSFET is often preferred when switching frequency is higher, reverse conduction is important or low-voltage resistive loss is favorable. There is no universal crossover voltage or frequency because semiconductor generation, die size, topology, temperature and cooling all move the boundary.
Design Condition
IGBT Implication
MOSFET Implication
Decision Check
High bus voltage and current
Moderate on-state voltage can be attractive.
RDS(on) and temperature drive conduction loss.
Compare total loss at actual current and temperature.
High switching frequency
Turn-off tail can make switching loss dominant.
Fast majority-carrier switching may reduce transition loss.
Calculate or measure switching energy.
Reverse current
Usually needs a separate or co-pack diode.
Body-diode and third-quadrant behavior are part of the device.
Review diode loss, recovery and dead-time path.
Short-circuit exposure
Specified withstand time may support DESAT shutdown.
Fault current can rise very quickly.
Match protection delay to the device fault limit.
Available cooling
Module and discrete packages offer different heat paths.
Parallel devices may spread loss but complicate sharing.
Estimate junction temperature for each candidate.
Compare the candidates over the real operating cycle rather than one nominal point. A motor drive may spend long periods at partial load and then experience short acceleration peaks. Include conduction loss, switching loss, diode behavior, driver power and cooling limits for those conditions. Choose the device that meets efficiency and temperature targets with acceptable waveform margin.
Which IGBT Ratings Determine Whether It Fits Your Circuit?
The decisive ratings are blocking voltage, current under real thermal conditions, on-state voltage, switching energy, gate charge, fault capability and thermal impedance. Every value must be read with its test conditions. A current rating measured at a controlled case temperature is not the current a sealed enclosure can deliver continuously.
Datasheet Item
What It Tells You
Required Design Input
Verification
VCES
Collector-emitter blocking limit
Maximum DC bus, regeneration and transient conditions
Measure worst-case overshoot with a suitable probe.
IC and pulsed current
Current capability under stated thermal limits
RMS, average and peak current waveforms
Apply temperature and pulse-duration derating.
VCE(sat)
On-state voltage at stated current, gate voltage and temperature
Conduction current and duty cycle
Use the curve nearest the real operating point.
Eon and Eoff
Energy dissipated during each transition
Bus voltage, current, frequency, RG and temperature
Match test conditions and confirm with waveforms.
QG and Miller charge
Charge the driver must source and sink
Target edge time and gate-voltage swing
Check peak drive current and gate waveform.
Rth(j-c) and Zth
Steady-state or transient heat transfer
Power-loss profile and cooling path
Calculate and measure junction-temperature margin.
SOA and short-circuit data
Permitted voltage-current-time stress
Fault current, starting temperature and shutdown time
Prove protection clears before the stated limit.
Also check the gate-emitter absolute maximum, recommended gate voltages, leakage current, internal diode data, isolation rating for modules, mounting torque and mechanical flatness. Use maximum ratings as boundaries, not operating targets. A design should preserve margin for production tolerances, temperature, aging and measured switching transients.
How Can You Estimate IGBT Loss and Junction Temperature?
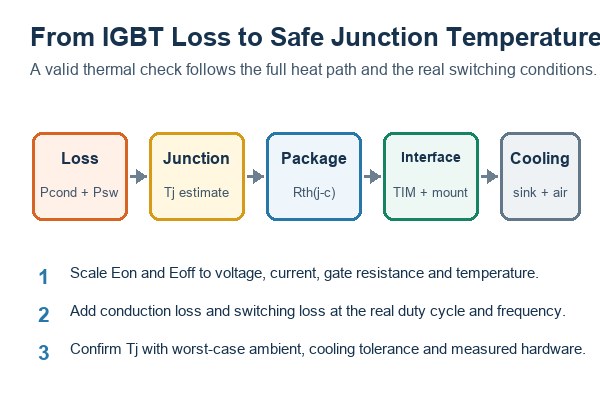
Estimate conduction and switching loss separately, add the other power-stage losses, and then apply the thermal path. This first-pass calculation shows whether the device and cooling concept are plausible. Final values require manufacturer curves at conditions close to the application and hardware measurements with safe probing.
Pcond ≈ VCE(sat) × IC × D
Psw ≈ (Eon + Eoff) × fsw
Consider a clearly hypothetical operating point: VCE(sat) is 1.9 V at 40 A, and the IGBT conducts for half the cycle. The first estimate is 1.9 × 40 × 0.5 = 38 W of conduction loss. If Eon + Eoff is 3.2 mJ at the intended voltage and current, switching at 10 kHz adds 0.0032 × 10,000 = 32 W of switching loss. The IGBT subtotal is about 70 W before diode, gate-driver, snubber and other losses.
Those numbers are an example, not a recommended operating point. A sinusoidal inverter has changing current, so calculate over the electrical cycle or use a validated simulation. Scale switching energy carefully for bus voltage, current, gate resistance and temperature. If the datasheet conditions differ substantially, a double-pulse test is the more reliable way to establish switching energy.
For a steady condition, a simplified junction estimate is:
Tj ≈ Tcase + Ploss × Rth(j-c)
If the example device dissipates 70 W and Rth(j-c) is 0.25 °C/W, the junction is about 17.5 °C above the measured case temperature. This does not include case-to-sink interface resistance or sink-to-ambient rise. For pulses, use transient thermal impedance rather than steady Rth. Validate the full chain at maximum ambient, worst airflow and realistic mounting pressure.
What Must an IGBT Gate Driver Control?
The driver must control gate voltage, peak source and sink current, switching speed, isolation and fault shutdown. A logic output alone rarely supplies the current or protection needed by a power IGBT. Select the driver after defining total gate charge, desired switching time, common-mode transient stress and the protection response.
A first estimate of transition current is IG ≈ QG/t. If total gate charge is 200 nC and the desired transition is 200 ns, the average current during that interval is about 1 A. The real peak can differ because gate current changes through the Miller plateau and the loop has resistance and inductance. Confirm the driver’s source and sink ratings at the actual supply voltage and temperature.
Gate-voltage range: use the recommended on and off values, not merely the absolute maximum. Observe the gate-emitter waveform at the device pins and verify that overshoot remains inside the limit.
Separate turn-on and turn-off control: different resistors or a diode-resistor network can balance turn-on loss against turn-off immunity. Record both resistor values with the measured switching result.
Miller immunity: high collector dV/dt can inject current through the Miller capacitance. A strong sink, Miller clamp, negative off voltage or lower-inductance gate loop can prevent false turn-on.
Isolation and common-mode behavior: choose insulation ratings and transient immunity for the system voltage and switching edge. Keep primary and secondary copper separated according to the applicable safety design.
Undervoltage lockout: prevent operation when the driver supply cannot enhance the IGBT correctly. Verify clean shutdown during both power-up and power-down.
Fault response: coordinate DESAT detection, blanking time, soft turn-off and controller reporting with the device’s short-circuit capability.
Place a gate-emitter resistor close to the device so the gate does not float if the driver is disconnected. Add a local gate clamp when the driver and layout cannot guarantee the voltage limit. These components should be selected from measured gate and collector waveforms, because overly aggressive clamping or resistance can slow fault response or increase switching loss.
How Should You Lay Out an IGBT Power Stage on a PCB?
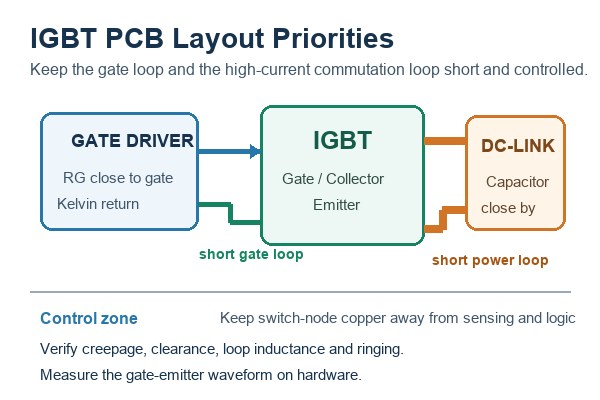
Minimize the gate loop and commutation loop, separate noisy switching copper from controls, and give current and heat predictable paths. Parasitic inductance converts rapid current change into voltage error and overshoot. A schematic can be correct while long loops make the hardware unstable or overstressed.
Place the driver beside the gate and emitter reference. Route the outgoing gate path and return together. The observable result should be a clean gate waveform without excessive ringing or bounce relative to the device emitter.
Use the Kelvin emitter when available. Keep the driver return separate from the power emitter until the package connection. This prevents load-current di/dt from changing the effective gate voltage.
Keep the DC-link capacitor close to the switching pair. The capacitor, high-side device and low-side device form the main commutation loop. Reducing its area lowers bus overshoot and ringing.
Control the switch-node area. Large high-dV/dt copper increases capacitive coupling. Keep it away from gate traces, current-sense inputs, isolation boundaries and low-level control circuits.
Route current-sense and protection signals as measurements. Use dedicated returns or differential routing where appropriate. Place DESAT and gate-clamp parts according to the driver’s loop requirements.
Design the copper and terminals for current and heat. Review RMS current, allowable temperature rise, copper thickness, via arrays, connector resistance and mechanical current sharing.
Add safe test access. Provide points for gate-emitter voltage, collector-emitter voltage, current and driver supplies. The probe connection must not create a larger loop than the circuit being measured.
Use measured waveforms to close the layout review. Excess collector overshoot points to commutation inductance, snubber selection or measurement error. Gate bounce during the opposite switch transition points to common-emitter inductance or Miller coupling. Repeated ringing at a fixed frequency suggests an LC resonance. Each observation should lead to a physical loop or component check before changing gate resistance by trial and error.
Which Protection Functions Prevent IGBT Failure?
Effective protection detects overcurrent, false turn-on, overvoltage, driver undervoltage and overheating before the device exceeds its time-dependent limit. A fuse can protect wiring and contain severe faults, but it is usually too slow to protect the semiconductor from a short circuit by itself.
Observed Stress
Likely Mechanism
Protection
Validation
Rapid current rise with high VCE
Load short circuit or shoot-through
DESAT or fast current trip with coordinated soft turn-off
Measure total detection and shutdown time.
Gate rises while commanded off
Miller current or common-emitter inductance
Strong sink, clamp, negative bias and Kelvin return
Observe the gate during the opposite transition.
Collector voltage overshoots
Stray inductance and fast di/dt
Tighter loop, controlled edge, clamp or snubber
Probe at the device under worst current and bus voltage.
Driver supply falls
Insufficient local energy or supply capacity
UVLO, local decoupling and suitable isolated supply
Check supply at the driver pins during switching.
Temperature exceeds target
Excess loss or inadequate cooling path
Temperature sensing, derating and controlled shutdown
Validate at maximum ambient and reduced airflow.
Protection thresholds and delays form a timing budget. Add current-sensor delay, DESAT blanking, digital filtering, isolator delay, driver response and turn-off time. The total must remain inside the device limit at the starting junction temperature. Test controlled fault cases with current-limited equipment and a written safety procedure instead of creating an unrestricted short circuit.
How Can You Test an IGBT Without Damaging the Circuit?
Begin with de-energized screening, then use current-limited functional tests before full-voltage switching tests. A multimeter may reveal an open gate, shorted collector-emitter path or abnormal diode junction, but it cannot prove switching energy, dynamic voltage margin, gate stability or short-circuit survival.
Make the system safe. Disconnect power, discharge the DC link, verify zero voltage with a rated instrument and follow the equipment’s lockout procedure. High-energy capacitors remain dangerous after input power is removed.
Inspect before measuring. Look for cracked packages, lifted terminals, discolored PCB areas, loose bus connections, damaged gate resistors and failed snubbers. A failed surrounding part may have caused the IGBT failure.
Screen the terminals. With the gate discharged, compare collector-emitter and gate-emitter readings with a known-good device or manufacturer guidance. A near-zero collector-emitter reading in both directions usually deserves further investigation.
Check the gate network. Measure the gate resistor, gate-emitter resistor, clamp and driver supply. Confirm there is no leakage path that keeps the gate partially charged.
Use a low-energy switching test. Apply a limited bus voltage and current, confirm correct driver timing and observe the gate and collector waveforms with properly rated differential or isolated probes.
Increase stress in controlled steps. Record overshoot, current, temperature and fault behavior at each step. Stop if the waveform exceeds the approved boundary or changes unexpectedly.
Do not test an IGBT in-circuit by randomly applying gate voltage. Parallel devices, bootstrap supplies, stored energy and controller interlocks can create unintended conduction. When a power stage fails, check the driver channel, opposing switch, current sensor, diode, snubber and DC-link capacitor before fitting a replacement.
What Should You Prepare Before Selecting an IGBT or Requesting a PCB Review?
Prepare the electrical stress profile, switching target, cooling conditions, protection timing and complete PCB design data. This turns device selection and DFM review into a checkable engineering task instead of a request for a generic “high-current IGBT.”
Electrical conditions: minimum, nominal and maximum DC-bus voltage; regeneration or surge behavior; RMS, average and peak current; duty cycle; topology and reverse-current path.
Switching conditions: target frequency, gate voltages, gate resistance, dead time, expected dV/dt and dI/dt, acceptable overshoot and EMI constraints.
Thermal conditions: ambient range, airflow, heat-sink or cold-plate details, interface material, mounting method, maximum case temperature and duty profile.
Protection conditions: current threshold, DESAT or comparator delay, soft-turn-off behavior, UVLO, overtemperature response and safe restart policy.
Mechanical and production data: device package, terminal current, creepage and clearance targets, enclosure limits, copper weight, board thickness, stackup and assembly process.
Review files: schematic, BOM with exact manufacturer part numbers, Gerber or ODB++ data, drill files, stackup, placement, mechanical drawing and relevant simulation or waveform results.
For a useful PCB review, mark the gate loop, commutation loop, switch node, isolation boundary and heat path in the design package. EBest Circuit can review those inputs for manufacturability and clarify PCB stackup, copper, via and assembly constraints before production. The review cannot replace device-level electrical or safety validation, so keep the operating assumptions and required test results with the released design.
Which IGBT Questions Still Need Quick Answers?
Q1: What does IGBT stand for?
A1: IGBT stands for insulated gate bipolar transistor. The name describes its insulated MOS gate and its bipolar conduction path.
Q2: Is an IGBT voltage-controlled or current-controlled?
A2: It is called a voltage-controlled device because gate-emitter voltage commands the state. The driver still supplies charging and discharging current during each transition.
Q3: What are the three IGBT terminals?
A3: The terminals are gate, collector and emitter. The gate controls the device, while the collector and emitter form the main power-current path.
Q4: Does an IGBT conduct reverse current?
A4: A conventional IGBT is mainly a unidirectional controlled switch. Reverse current usually flows through a separate or co-pack freewheel diode, so confirm the module circuit.
Q5: Can a microcontroller drive an IGBT directly?
A5: Usually not in a practical power stage. An IGBT normally needs a dedicated gate driver for peak current, voltage level and isolation, plus UVLO and fault shutdown.
Q6: Why is a gate resistor necessary?
A6: It controls gate current and switching speed. Its value changes switching loss, overshoot, ringing and EMI, so confirm it with measured gate and collector waveforms.
Q7: What does VCE(sat) mean?
A7: It is the collector-emitter voltage while the IGBT is on under stated conditions. Use it with current and duty cycle for a first conduction-loss estimate.
Q8: Why does an IGBT have tail current?
A8: Stored carriers remain after the gate channel turns off. Their removal creates tail current, which adds turn-off time and switching energy.
Q9: Does every IGBT need negative gate voltage when off?
A9: No. The need depends on Miller coupling, driver sink strength and loop inductance. Follow the device and driver guidance, then verify off-state gate margin during the opposite switch transition.
Q10: What is the most common IGBT PCB layout mistake?
A10: A common mistake is allowing the gate or commutation loop to become too large. The resulting parasitic inductance can cause gate bounce, overshoot, ringing and false turn-on.
An effective insulated gate bipolar transistor design is a chain of linked decisions. Select the switch from the real electrical and thermal profile, size the driver from gate charge and timing, control the physical loops, and prove protection with measured waveforms. When those inputs are documented before PCB release, manufacturing review and hardware validation become much more reliable.
Need help sourcing the components for your IGBT power stage? Send EBest Circuit your BOM with manufacturer part numbers, approved alternatives, required quantities, target delivery date and traceability requirements. Our component sourcing team can review availability and substitution constraints together with your PCB or PCBA requirements and prepare a quotation. Contact us with your BOM to start the component procurement review.
This website uses cookies to enhance your experience, remember your preferences, and help us understand how visitors use our site. You can accept all cookies, reject non-essential cookies, or manage your settings.
This website uses cookies to improve your experience while you navigate through the website. Out of these cookies, the cookies that are categorized as necessary are stored on your browser as they are essential for the working of basic functionalities of the website. We also use third-party cookies that help us analyze and understand how you use this website. These cookies will be stored in your browser only with your consent. You also have the option to opt-out of these cookies. But opting out of some of these cookies may have an effect on your browsing experience.
Necessary cookies are absolutely essential for the website to function properly. These cookies ensure basic functionalities and security features of the website, anonymously.
Cookie
Duration
Description
cookielawinfo-checkbox-analytics
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytics".
cookielawinfo-checkbox-functional
11 months
The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional".
cookielawinfo-checkbox-necessary
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Necessary".
cookielawinfo-checkbox-others
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Other.
cookielawinfo-checkbox-performance
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance".
viewed_cookie_policy
11 months
The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data.
Functional cookies help to perform certain functionalities like sharing the content of the website on social media platforms, collect feedbacks, and other third-party features.
Performance cookies are used to understand and analyze the key performance indexes of the website which helps in delivering a better user experience for the visitors.
Analytical cookies are used to understand how visitors interact with the website. These cookies help provide information on metrics the number of visitors, bounce rate, traffic source, etc.
Advertisement cookies are used to provide visitors with relevant ads and marketing campaigns. These cookies track visitors across websites and collect information to provide customized ads.