PCB manufacturing PCB manufacturing
Home > Blog

BGA Escape Routing

BGA Escape Routing Rules and Methods: Fanout, Vias, and Layer Planning
Wednesday, September 30th, 2026

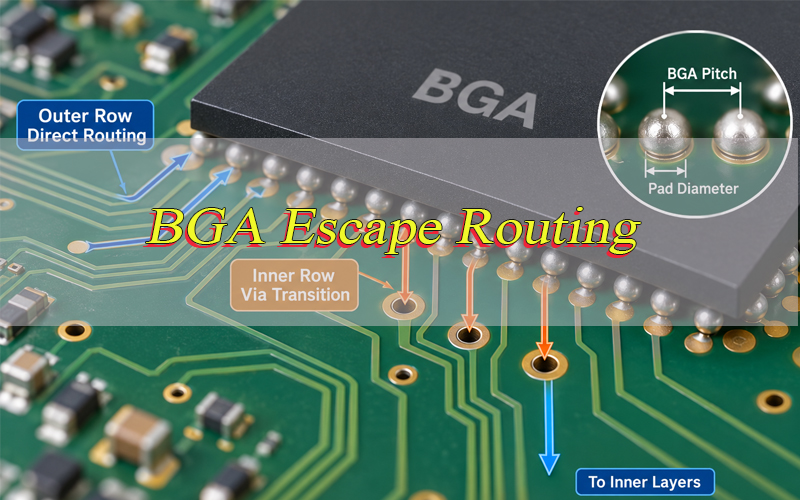
BGA escape routing moves signal, power, and ground connections from beneath a BGA package into usable PCB routing channels. The design is mainly controlled by BGA pitch, pad size, trace and spacing capability, via geometry, ball density, and PCB stackup. These constraints should be defined before detailed routing begins, especially for FPGAs, processors, SoCs, and memory devices.
BGA Escape Routing, https://www.bestpcbs.com/blog/2026/09/bga-escape-routing/

What Is BGA Escape Routing?

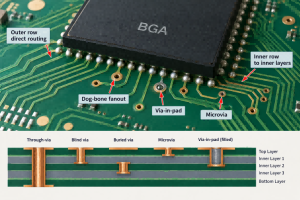
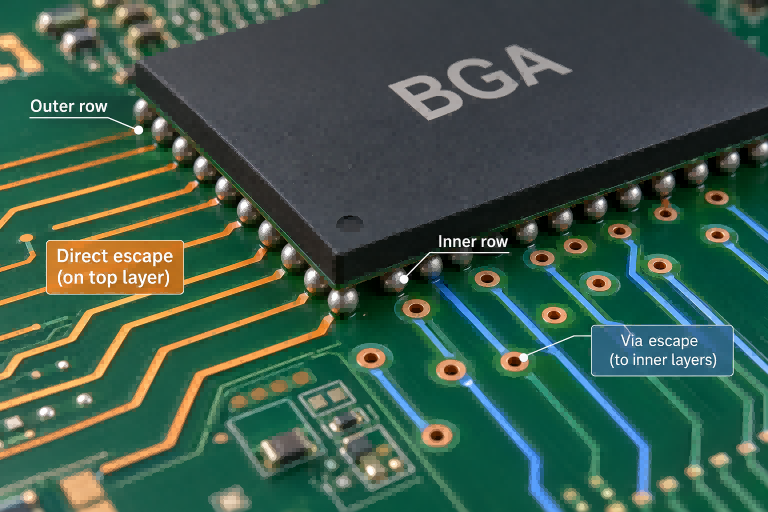
BGA escape routing is the process of bringing connections out of the BGA ball field so they can continue across the PCB. Outer ball rows can often escape directly on the component layer, while inner rows usually require vias to reach additional signal layers.

BGA fanout is one part of this process. Fanout describes the transition from a BGA pad to a trace or via, while BGA escape routing covers the complete breakout from the ball field into open routing space. As the pitch decreases and the row count increases, routing channels become narrower and the via strategy becomes more critical.

What Design Constraints Define a BGA Escape Routing Strategy?

Before choosing a fanout method, check the package geometry and PCB fabrication limits together:

  • BGA pitch: Smaller pitch reduces the space available for traces and vias.
  • Pad diameter: Larger lands leave narrower routing channels.
  • Trace width and spacing: Determine how many traces can pass between pads.
  • Via geometry: Large via pads can block inner-row escape paths.
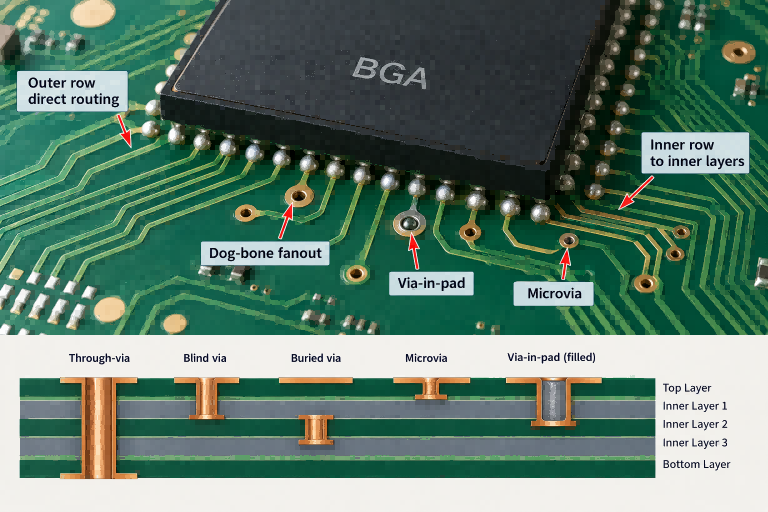
  • Via structure: Through-vias, blind vias, microvias, and via-in-pad structures provide different layer access.
  • PCB stackup: Defines the available routing layers and reference planes.
  • Fabrication limits: Set practical trace, spacing, drill, annular ring, and microvia rules.

These values cannot be optimized separately. A narrower trace does not solve the layout if the fanout vias still occupy the channel. Confirm the footprint, trace and spacing rules, via dimensions, and stackup before the BGA breakout is finalized.

How Does BGA Pitch Affect the Escape Routing Method?

BGA pitch determines how much room is available between adjacent lands. Larger-pitch packages usually provide enough space for conventional dog-bone fanout and mechanically drilled vias. As the pitch decreases, via pads and trace clearances begin competing for the same space.

BGA PitchTypical ApproachMain Constraint
1.27 mmDog-bone and through-viaUsually generous routing space
1.0 mmDog-bone and through-viaVia and trace clearance
0.8 mmOptimized dog-bone or smaller viaFewer routing channels
0.65 mmSmall via, HDI, or via-in-padInner-row access
0.5 mm and belowMicrovia and via-in-pad often consideredVery limited breakout space

These are planning ranges rather than fixed rules. A simple 0.8 mm package may route with standard through-vias, while a dense FPGA at the same pitch may not. Ball count, number of rows, signal assignment, trace and spacing rules, and available routing layers matter as much as pitch.

How Do You Determine Whether Traces Can Pass Between BGA Pads?

Start with the physical space between adjacent PCB lands. If the ball pitch is P and the land diameter is D:

Available pad gap = P – D

For one trace to pass through that gap, the trace width plus twice the required clearance must fit within the available pad gap.

If two traces must share the same channel, the required trace-to-trace spacing must also be included. This simple check quickly shows whether the intended breakout is realistic before the full BGA fanout is created.

The calculation is only a starting point. Copper thickness, etching tolerance, registration, and actual fabrication capability reduce the usable margin. A trace that fits mathematically is not automatically a reliable production rule. Avoid designing every channel at the minimum trace and spacing limit unless the routing density requires it.

How Do You Route the Outer Rows of a BGA?

Outer rows normally provide the easiest paths out of the package. The goal is to use that advantage without blocking the deeper rows.

  • Route directly outward where possible: Avoid unnecessary vias when a connection can remain on the component layer.
  • Preserve inner routing channels: Do not fill valuable space with easy outer-row connections before the deeper rows are planned.
  • Escape toward the destination: Route toward nearby memory, connectors, processors, or other ICs when placement is already defined.
  • Keep sensitive nets short: Avoid unnecessary width changes and layer transitions.

Direct routing is useful, but it should still follow the complete BGA escape routing plan. The easiest connection should not occupy the only practical path available to a more constrained signal.

How Do You Escape the Inner Rows of a BGA?

Inner rows are blocked by surrounding balls, so most of their connections must transition to another layer before leaving the package area.

A practical sequence is:

  • Plan the deepest rows first: Reserve their escape channels before easier signals use the available space.
  • Move signals to internal layers: Use through-vias, blind vias, or microvias where appropriate.
  • Assign layers by routing capacity: Do not rely on a fixed one-row-per-layer assumption.
  • Reserve space for power and ground vias: These connections also consume breakout area.
  • Change the via strategy when necessary: If conventional via pads occupy too much space, consider via-in-pad or microvias.

There is no universal rule that a certain number of BGA rows requires a fixed number of PCB layers. The required layer count depends on the actual pad, via, and trace geometry.
BGA Escape Routing, https://www.bestpcbs.com/blog/2026/09/bga-escape-routing/

When Should You Use Dog-Bone Fanout for BGA Escape Routing?

Dog-bone fanout connects a BGA land to a nearby via with a short trace. It works well when the pitch provides enough room for the connection and the via pad does not block the channels required by surrounding signals.

This method is common with larger-pitch packages and many 1.0 mm or 0.8 mm BGAs because conventional drilled vias can often be used without pushing the PCB process to aggressive limits. It also keeps the via outside the solder land, simplifying fabrication compared with via-in-pad.

The limitation appears when the via field becomes denser than the available routing channels. Once conventional fanout vias begin blocking the paths required by deeper rows, via-in-pad or microvias are usually more effective than continuing to shrink the dog-bone geometry.

When Should You Use Via-in-Pad for BGA Escape Routing?

Via-in-pad becomes useful when a conventional fanout via occupies too much space beside the BGA land or prevents access to deeper rows. Placing the via directly in the land frees routing space between adjacent pads and allows an immediate layer transition.

This approach is common in fine-pitch FPGA, processor, SoC, memory, and other high-density BGA layouts. It can also shorten the pad-to-via transition for high-speed signals.

The via normally needs to be filled and planarized for BGA assembly. An open via inside the solder land can draw solder into the hole during reflow and reduce the solder volume at the joint. Via-in-pad therefore adds fabrication steps, but it is justified when it solves a real routing-density or signal-transition problem.

When Are Microvias Needed for Fine-Pitch BGA Escape Routing?

Microvias are used when conventional mechanically drilled vias occupy too much area. Their smaller geometry allows signals to move between nearby PCB layers while leaving more routing space for other connections.

They are especially useful in HDI BGA escape routing where via-in-pad is combined with blind microvias. Instead of carrying a large through-via through the entire stackup, a signal can transition only to the layer where it needs to be routed.

Microvias may be stacked or staggered depending on the layer structure and routing density. Their use should be driven by routing requirements rather than BGA pitch alone. If conventional vias still provide enough escape space, adding microvias only increases fabrication complexity.
BGA Escape Routing, https://www.bestpcbs.com/blog/2026/09/bga-escape-routing/

How Many PCB Layers Do You Need for BGA Escape Routing?

Layer count depends on how many signals must leave the BGA and how much routing capacity each layer provides. Pitch alone cannot determine the required stackup.

A dense device may require more routing layers because of high ball count, limited trace channels, power and ground planes, controlled-impedance nets, differential pairs, and high-speed interfaces. Outer signals may remain on the component layer, while deeper rows move to different internal layers.

DDR, PCIe, USB, Ethernet, MIPI, and SerDes connections may also require specific reference planes, so their layer allocation cannot be based only on available routing space.

Use enough layers to complete the breakout without forcing the entire BGA area to minimum fabrication rules. In some designs, one additional signal layer provides better production margin than aggressive trace and via reduction across several layers.

How Should You Escape Differential Pairs From a BGA?

Differential pairs should leave the BGA with similar geometry on both sides of the pair. Their breakout length, via type, antipad geometry, and reference environment should remain as consistent as the package allows.

If a layer transition is required, both members should normally use equivalent vias and share the same reference structure. Avoid giving one side an extra via or a significantly longer escape path.

Detailed length tuning is better performed once the pair reaches open board space. Inside the BGA field, maintaining pair symmetry and a clean return path is more useful than forcing exact length matching with unnecessary meanders.

For PCIe, USB, Ethernet, MIPI, and SerDes interfaces, the breakout should be planned together with controlled impedance, reference-plane continuity, and via transition design.

How Should Power and Ground Balls Be Handled During BGA Escape Routing?

Power and ground connections should be planned at the same time as the signal fanout. Leaving them until the end can create a breakout that works for signals but performs poorly for power delivery.

Power balls should have short connections to their planes, with enough via capacity for the expected current. Ground vias should also be available near high-speed signal transitions so the return current can follow a short path when a signal changes reference layers.

Decoupling capacitors affect the same area. Their connections should remain short and direct rather than being forced around an already congested fanout. Signal escape, power delivery, ground return, and decoupling placement should be treated as one routing problem.

What BGA Escape Routing Mistakes Should You Avoid?

Most BGA breakout problems result from using the available space in the wrong order or choosing geometry before checking the complete routing path.

  • Oversized fanout vias: Block channels required by deeper rows.
  • Unsupported trace and spacing rules: Create DFM problems or reduce production margin.
  • Routing easy nets first: Can trap inner-row signals.
  • Open via-in-pad: Can draw solder away from the BGA joint.
  • Late stackup definition: Forces routing and reference-plane changes later.
  • Too many layer transitions: Add vias and high-speed discontinuities.
  • Broken return paths: Increase signal integrity and EMI risk.
  • Poor differential symmetry: Introduces unnecessary skew.
  • Blocked power access: Leaves insufficient room for power and ground vias.
  • Minimum rules everywhere: Makes production less tolerant of normal process variation.

Solve the most constrained areas first, then use the remaining channels for less difficult connections.

What Should You Verify Before Releasing a BGA PCB for Fabrication?

Passing PCB DRC is not enough. The completed BGA escape routing should also match the intended fabrication and assembly process.

  • BGA footprint: Verify pitch, pad diameter, orientation, and solder mask geometry.
  • Trace and spacing: Check the smallest neck-down and copper clearance.
  • Via geometry: Verify drill diameter, pad size, annular ring, antipad, and layer span.
  • Via-in-pad: Confirm filling, plating, and planarization requirements.
  • Microvias: Verify the layer span and stacked or staggered construction.
  • PCB stackup: Check routing layers, dielectric thickness, and reference planes.
  • High-speed nets: Verify impedance, differential symmetry, and return paths.
  • Power delivery: Check plane access, via quantity, and decoupling paths.
  • Manufacturing margin: Maintain sufficient tolerance beyond absolute process limits.

For HDI, fine-pitch BGA, via-in-pad, and microvia designs, a DFM review before fabrication can identify breakout and stackup conflicts before they reach production.

FAQs About BGA Escape Routing

Q1: Can FPGA pin swapping make BGA routing easier?

A1: Yes, when the FPGA architecture allows it. Reassigning compatible I/O pins can reduce trace crossings and improve escape direction. Pin changes must still respect I/O banks, voltage domains, differential-pair assignments, clock-capable pins, and device-specific restrictions.

Q2: Should unused or NC BGA balls still have PCB pads?

A2: Usually yes. Follow the recommended land pattern unless the component documentation allows a change. Removing an NC pad only to create more routing space may affect assembly or future device compatibility. Do not alter the footprint without package-specific guidance.

Q3: Does copper thickness affect BGA breakout capability?

A3: Yes. Heavier copper generally requires more allowance during etching, making very fine trace and spacing geometry harder to produce. Copper thickness should be considered when setting routing rules beneath a dense BGA.

Q4: Does solder mask design matter around BGA pads?

A4: Yes. Solder mask registration and pad definition affect the usable area around each land. The mask design should support reliable assembly while maintaining realistic fabrication tolerance. Do not reduce mask clearances only to gain routing space.

Q5: Can BGA escape traces use a local neck-down?

A5: Yes. A short neck-down can help a trace pass through a restricted breakout channel and then return to its normal width outside the BGA. Keep the narrow section short and check its impedance or current-carrying requirements where relevant.

Q6: Should test points be placed inside the BGA breakout area?

A6: Usually not unless the available space clearly supports them. Test pads consume routing space and can increase congestion around already constrained signals. Place test access outside the dense ball field whenever practical.

Q7: Can thermal vias interfere with BGA routing?

A7: Yes. Thermal vias near the package can occupy channels required by signals, power, or ground connections. Plan thermal management and BGA routing together so thermal structures do not block critical breakout paths.

Q8: Does BGA breakout affect EMI performance?

A8: It can. Long escape paths, poor reference continuity, unnecessary layer changes, and large return loops can increase unwanted radiation. Short routes and continuous return paths help reduce EMI risk around high-speed BGA interfaces.

Q9: Can buried vias reduce congestion around a BGA?

A9: Yes. Buried vias connect internal layers without occupying every layer in the PCB stackup, which can free routing space elsewhere. They also increase fabrication complexity, so use them only when the routing benefit justifies the additional process steps.

Q10: How does nearby component placement affect BGA routing?

A10: Placement determines where major signal groups should leave the package. Memory, connectors, decoupling capacitors, and adjacent ICs should be positioned so related nets can escape in useful directions. Good placement can reduce crossings, vias, and unnecessary routing length.

Q11: Can BGA congestion be reduced before routing begins?

A11: Yes. Review the pin map, interface direction, component placement, stackup, and signal grouping before detailed fanout. Programmable devices may also allow legal pin reassignment. Early planning is usually more effective than repairing blocked routes later.

Q12: Does dense BGA routing make rework harder?

A12: It can. Fine pitch, via-in-pad, dense neighboring components, and limited access can all increase rework difficulty. Adequate component clearance and stable pad and via construction help reduce rework risk.

Conclusion

Effective BGA escape routing depends on available routing space, via geometry, and PCB stackup. Plan the inner rows first, use conventional fanout where it fits, and move to via-in-pad or microvias when routing density requires them.

For fine-pitch BGA, HDI, via-in-pad, microvia, or high-layer-count PCB projects, EBest Circuit can review your Gerber files, stackup, BGA pitch, via structure, and impedance requirements before production. Contact sales@bestpcbs.com for technical review and quotation.
You may also like

How Does BGA PCB Design Support Reliable Fanout, Routing and Assembly?
Thursday, August 27th, 2026

BGA PCB design succeeds when the package, fanout, stack-up, electrical constraints and manufacturing route are treated as one connected decision. A breakout that looks clean on screen can still fail if the land pattern uses the wrong package revision, the via structure is unavailable, return paths are broken, or hidden joints cannot be inspected. The design process must turn the exact ball map into a buildable PCB and assembly plan, supported by the data that EBest Circuit needs to review and quote the project.

BGA PCB Design, engineer reviewing a dense BGA breakout before PCB fabrication

What Should Be Checked Before Starting BGA PCB Design?

Start only after the exact package identity, ball map and manufacturing limits are controlled. BGA pitch is not enough to create a land pattern or choose a stack-up. The same nominal pitch can appear on packages with different ball diameters, depopulated regions, power fields, body sizes and vendor recommendations.

The design input set should answer six practical questions:

  • Which package revision is being placed? The controlled record includes the full manufacturer part number, package code, drawing revision and approved pinout. A footprint copied from a similar device is not proof of compatibility.
  • Where are the critical balls? Mark high-speed groups, clocks, differential pairs, memory interfaces, power, ground, sense pins, no-connects and reserved locations before choosing escape directions.
  • What does the component vendor recommend? Reconcile the vendor’s board-land and routing guidance with the intended PCB and assembly processes.
  • What can the proposed fabricator build? The capability review covers trace and spacing, drill structure, microvia spans, via filling, registration, copper weights and stack-up options.
  • What must the assembler control? Assembly inputs cover solder-mask registration, stencil needs, package handling, thermal-profile constraints, neighboring-component clearance and hidden-joint inspection access.
  • How will success be verified? Establish the electrical, thermal and assembly acceptance evidence before routing removes test access or forces an unsuitable inspection plan.

When an input remains provisional, label it as an open decision. That prevents an early routing assumption from silently becoming a released manufacturing requirement.

How Does BGA Pitch Affect Pad, Trace and Via Selection?

Pitch controls the physical space between balls, but it does not select the land, trace or via by itself. The usable routing channel also depends on the approved land diameter, solder-mask opening, copper tolerance, trace width, clearance and via geometry. A pitch value therefore cannot prove that a board needs HDI or that a particular trace width will fit.

Pad style belongs in the same decision. With a non-solder-mask-defined land, the mask opening is larger than the copper land and leaves the copper edge exposed. With a solder-mask-defined land, the mask opening defines the exposed soldering area. Neither style is universally better. The package recommendation, land geometry, mask registration, surface finish and assembly process determine which choice is appropriate.

As the available channel becomes tighter, ask the questions in this order:

  • Pad: Does the land pattern match the exact package and the intended assembly process?
  • Mask: Can the fabricator hold the required opening and web without creating registration or mask-sliver risk?
  • Trace: Can a route pass through the remaining channel with the required clearance and electrical performance?
  • Via: Is there space for a dog-bone transition, or must the via move into the land or use a build-up layer?
  • Stack-up: Does the selected trace and via geometry still work with the impedance, copper and dielectric structure?

The deliverable is a manufacturer-reviewed geometry set for the BGA region, based on its actual package and fabrication constraints.

When Should You Use Dog-Bone, Microvia or Via-in-Pad Fanout?

The preferred fanout is the least complex structure that can escape the required balls and meet the design constraints. The decision is conditional: pitch affects the available space, but ball-map density, trace rules, stack-up access and reference continuity decide which structure actually works.

  • Dog-bone fanout: This fits a package when a short trace can connect the land to a nearby plated through via without violating the land, mask, trace or clearance rules. It is often the most economical route, but the through via occupies space and creates antipads on every penetrated layer.
  • Blind microvias: These fit inner rows that need denser escape when selected build-up layers provide enough routing access. The fabricator must confirm drill depth, capture lands, registration, copper filling and the permitted stacked or staggered structure.
  • Via-in-pad plated over: This fits a layout when moving the transition into the BGA land provides needed escape density or a shorter electrical path. The via must be specified as a controlled filled, planarized and plated feature so the soldering surface is flat.
  • Buried or combined via structures: These make sense only when the layer transition plan justifies the additional lamination and registration complexity. Adding every available via type without a clear routing purpose increases cost and failure opportunities.

A common mistake is to select via-in-pad because the package is described as fine pitch, then discover that the proposed shop cannot build the specified fill or layer span. The opposite mistake is forcing through vias into a dense field and losing the power-plane area or signal channels needed on deeper layers. A fabricator review of a sample fanout should occur before the rest of the device is completed.

BGA PCB Design, engineer comparing dog-bone microvia and via-in-pad fanout options

How Many PCB Layers Are Needed for BGA Escape Routing?

There is no reliable layer-count formula based only on ball count or pitch. Layer demand comes from the number and location of balls that must escape, the channels opened by the chosen fanout, route direction, reference-plane needs, power distribution and the fabrication structure.

Begin with a marked ball map. Assign perimeter signals that can leave on surface layers, identify inner rows that require vias, reserve paths for critical interfaces, and keep power and ground fields visible rather than counting them as ordinary signals. Next, sketch the escape direction for each signal layer and check whether the adjacent reference remains continuous.

For example, adding a routing layer may not solve congestion if through-via antipads still block the same channels. A blind-via build-up may release those channels, but it changes lamination, cost and allowable layer transitions. A useful stack-up estimate therefore shows:

  • which ball groups leave on each signal layer;
  • which plane provides the return path for that layer;
  • where signals change reference layers and need nearby ground transitions;
  • how much plane copper is removed by via pads and antipads;
  • which via spans and impedance structures the fabricator has accepted.

The stack-up can be closed after a representative inner-row breakout passes routing, plane-integrity and manufacturing review. This verification exposes residual congestion risk and avoids paying for extra layers that do not add usable escape capacity.

How Should BGA Escape Routing Protect Signal Integrity?

The breakout is part of the electrical channel and needs the same constraint discipline as the main route. Narrow neck-down traces, via barrels, antipads, reference changes and crowded return paths can create discontinuities before a signal reaches its normal controlled-impedance geometry.

A differential pair needs a symmetric escape path. Unequal fanout routes, different layer-change locations or a split reference can add skew and mode conversion while forcing return current onto a longer path. Reserve comparable transitions for both members and keep a continuous reference with nearby return vias.

The same cause-and-effect check applies to other interfaces:

  • A long unused through-via stub can become electrically significant on a bandwidth-sensitive channel; model it and consider a different via span or backdrilling when justified.
  • An abrupt neck-down changes impedance; include the actual breakout geometry in the channel model instead of assuming the main-route width represents the whole interconnect.
  • A dense via field can create reference-plane voids and coupling between transitions; inspect antipad interaction, return-via placement and local plane continuity.
  • Routing critical lanes last may force avoidable transitions and detours; reserve their channels before low-speed nets consume them.

The relevant loss, impedance, skew and transition limits come from the component or interface design guide. Geometry that is acceptable for a control signal may not be acceptable for a clock, memory strobe or high-speed serial lane.

How Should Power, Ground and Decoupling Be Planned Under a BGA?

A BGA can escape every signal and still have an inadequate power-distribution network. Power and ground balls need short, distributed transitions into usable plane copper, and each decoupling connection needs a low-inductance current loop appropriate to its rail.

A complete rail map identifies every supply, ground, analog rail, sense connection and reserved power pin in the approved ball map. The via field can then be reviewed as a current path rather than a routing obstacle. Too few power vias can concentrate current; oversized antipads can narrow a plane; poorly placed signal transitions can divide the copper that the package needs.

  • At the package: distribute power and ground vias across the corresponding ball fields instead of collecting a rail through one narrow exit.
  • At the planes: inspect the copper remaining after antipads, clearances and route channels are applied.
  • At the capacitors: minimize the loop formed by the supply terminal, its via, the plane pair, the return via and the ground terminal within the available placement area.
  • At transitions: add return vias near signal layer changes so return current does not detour around plane openings.
  • At verification: evaluate voltage drop and impedance using the real stack-up, device current profile and capacitor models where the product risk requires it.

A fixed capacitor count or distance is not a substitute for this analysis. Package inductance, rail targets, capacitor behavior, mounting geometry and board construction all affect the result.

How Can BGA PCB Design Reduce Thermal and Warpage Risk?

Thermal and mechanical decisions should control device temperature without creating board bending or solder-joint strain. More copper and more thermal vias may improve heat spreading, but an asymmetric copper field or a heavy local structure can also change board stiffness and warpage.

The thermal review starts with the approved power and operating case, then follows the heat path through package lands, board copper, thermal vias, planes, airflow and any heat-spreading interface. Its interaction with the rest of the board includes:

  • Copper balance: large local plane differences and uneven panel copper can contribute to bow and twist, so review distribution with the fabricator.
  • Via placement: thermal vias should support the intended heat path without removing excessive plane copper or disrupting signal return paths.
  • Board support: mounting points, connectors and stiffeners should not impose bending loads through the BGA region during assembly or service.
  • Component neighborhood: tall parts, shields and connectors can block airflow or rework access and can impose a different thermal mass during soldering.
  • Reflow behavior: the assembler should develop the profile for the actual package and board rather than reusing a profile from a smaller or less massive assembly.

High-risk products may require temperature measurement, warpage characterization, strain measurement or environmental testing. The applicable method and limit should come from the component, product or validated process requirement, not from a generic BGA claim.

Which DFM Checks Should Be Completed Before BGA PCB Fabrication?

DFM should prove that the released design can be fabricated and assembled as specified before tooling begins. This chapter owns pre-production corrections; it does not use later X-ray images as a substitute for closing design errors.

  • Footprint identity: compare copper lands, solder-mask openings, paste intent, courtyard and orientation marks with the exact package revision.
  • BGA-region geometry: run the proposed shop’s trace, spacing, annular-ring, drill-to-copper and mask-registration rules on the real fanout.
  • Via construction: document drill type, layer span, fill, planarization, plating and any backdrill requirement. The stack-up must support every transition.
  • Stack-up and impedance: obtain a manufacturable material and copper proposal, then update the controlled geometry rather than releasing an unconfirmed nominal stack-up.
  • Plane and return paths: review antipad fields, splits, necked power areas and reference changes under and around the package.
  • Assembly access: check stencil feasibility, neighboring clearances, component orientation, fiducials, thermal mass, rework envelope and access for the planned inspection method.
  • Data consistency: compare fabrication output, drill data, assembly drawing, BOM and placement data against the same design revision.

Each open item needs an owner and a disposition in the released files. A verbal shop-floor workaround may solve one build but leaves the next lot exposed to the same ambiguity.

What Assembly Controls Reduce BGA Soldering Defects?

Good assembly control begins with board data that allows consistent paste transfer, placement and heating. The design-related controls below address PCB and package decisions that change the risk of opens, bridging, voiding, head-in-pillow and rework damage.

Paste deposition: land geometry, via-in-pad flatness, stencil design and local board topography affect the amount and uniformity of paste delivered to the joint. An open or depressed via in a solder land can pull solder away from the interface.

Placement and handling: clear orientation marks, usable fiducials, controlled package moisture handling and adequate neighboring clearance reduce placement and rework errors. If underfill or reinforcement is required, its access and inspection consequences need to be considered during layout.

Thermal profile: package size, board copper, shields and nearby thermal masses influence heating across the BGA. The assembler should validate the profile on the representative build rather than assuming that one profile fits every board.

Change control: substitutions in package code, surface finish, stencil, paste, board supplier or via construction can change soldering behavior. These changes remain tied to an approved revision and trigger the affected process verification again.

How Should BGA Solder Joints Be Inspected and Tested?

A risk-based combination of process records, imaging and electrical tests provides stronger evidence. No single method proves every hidden-joint condition, and not every PCBA needs every inspection method.

  • SPI can confirm solder-paste deposition before placement when the process plan includes it, helping catch volume or alignment problems before the joints become hidden.
  • AOI can verify visible placement, polarity and nearby solder features, but it cannot directly see the full joint field beneath a BGA.
  • X-ray can reveal selected hidden features such as alignment, bridging patterns and void distribution. The plan should state the required views, observable features, acceptance criteria and sampling.
  • ICT, flying probe or boundary scan can provide electrical coverage when the design exposes meaningful access or device support.
  • Functional testing checks behavior at product level against an approved procedure, but a passing function does not explain every latent solder condition.
  • Cross-section or dye-and-pry may support qualification or failure analysis when non-destructive evidence cannot resolve the cause.
BGA PCB Design, X-ray review of hidden BGA solder joints after assembly

When a defect is found, the corrective action should connect it back to the design and process evidence. A change to the land, via fill, stencil, profile, board support or package handling needs to answer the observed failure mechanism and produce evidence on the next build.

What Files Are Needed for BGA PCB Manufacturing and Assembly?

A manufacturer can review and quote the project accurately only when the package, PCB, assembly and test data describe the same revision. The review package therefore contains enough information to reproduce the intended product rather than only a screenshot of the BGA breakout.

  • Component and package data: manufacturer part number, package drawing, ball map, land guidance, thermal data and device-specific PCB instructions.
  • PCB design data: native layout or agreed intelligent exchange, schematic, net classes, constraints and controlled library identity.
  • Fabrication package: Gerber or ODB++, drill files, drawing, stack-up, material notes, copper, impedance targets, via construction and acceptance criteria.
  • Assembly package: controlled BOM, centroid or placement data, assembly drawing, polarity/orientation information, stencil notes and any approved substitutions.
  • Inspection and test requirements: required X-ray views or criteria, test method, test files, fixtures, programming data and expected records.
  • Commercial inputs: prototype and production quantities, panel or delivery preference, schedule target, packaging, traceability and documentation needs.

A quote should show what is included across PCB fabrication, components, BGA assembly, tooling, inspection, testing, special processes, packaging and freight. The lowest unit price is not the lowest project cost if essential controls or one-time items are omitted.

How Can EBest Support Fine-Pitch BGA PCB Manufacturing and Assembly?

EBest Circuit can review and quote a connected route from PCB DFM through fabrication, component sourcing, BGA assembly and agreed verification. The land pattern, via structure, stack-up and assembly requirements can then be resolved against one controlled data package before production decisions become expensive to change.

  • DFM review: fewer late manufacturing changes. The returned findings identify open pad, mask, via, clearance and data-consistency issues from the package drawing, ball map, stack-up and layout before tooling.
  • PCB fabrication: a route matched to the fanout. The quoted stack-up and via construction can be checked against the actual breakout instead of treating HDI, via-in-pad or backdrilling as labels.
  • Component sourcing: controlled package identity. The BOM and approved manufacturer part number keep the assembled package aligned with the footprint and ball map used in design.
  • BGA assembly: design and process coordination. Stencil, via-in-pad surface, placement access, package handling and thermal-profile needs can be reviewed with the board data.
  • Applicable X-ray: hidden-joint evidence. Where the package and risk plan require it, the quotation can state the inspection scope and expected output instead of assuming that a generic X-ray statement is sufficient.
  • Agreed testing: product-specific coverage. The intended ICT, flying-probe, programming or functional-test inputs allow feasibility and deliverables to be confirmed before the order.

This support remains project specific. Final pad dimensions, via structures, process controls and inspection criteria depend on the component, board design and approved customer requirements.

FAQs About BGA PCB Design

These answers address common boundary questions without turning them into universal layout rules. The final decision still belongs to the actual package, board stack-up and manufacturing route.

Q1: What BGA pitch is considered fine pitch?

A1: No single pitch threshold determines the PCB process. The usable pad, mask, trace and via geometry, together with the ball map and supplier capability, matters more than a label.

Q2: Can a 0.5 mm pitch BGA be routed without HDI?

A2: It is possible on some packages and board builds. Depopulated regions, outer-row access, allowed trace and spacing, land size and the exact pinout can make a conventional route practical; dense inner rows may still require microvias or via-in-pad.

Q3: Can plugged vias be placed under a BGA?

A3: Yes, when the approved via structure creates the required soldering surface. The fabricator must control the fill, planarization and plating; an unspecified plug is not equivalent to plated-over via-in-pad.

Q4: Is ENIG suitable for BGA assembly?

A4: ENIG can be suitable when its specification and process match the assembly. Select the surface finish with shelf-life, soldering, planarity and product requirements rather than by package name alone.

Q5: Can 3 mil traces be used for BGA escape routing?

A5: Only when the fabricator accepts the geometry and it meets the design requirements. Copper, clearance, impedance and reliability still apply; a width used in one stack-up should not become a universal rule.

Q6: Why does via-in-pad increase PCB cost?

A6: It can add several controlled fabrication operations. Drilling, filling, planarization, plating, inspection and possibly sequential lamination depend on the via span, board build and supplier process.

Q7: Can a BGA be reworked after assembly?

A7: Rework may be possible when the layout and an approved process permit it. Review component access, neighboring clearances and board thermal behavior before release, especially on dense or thermally massive boards.

Q8: Can AOI inspect BGA solder joints?

A8: AOI cannot directly see the hidden joint field. It can check visible placement and surrounding features, while hidden joints normally require another method such as X-ray plus appropriate electrical evidence.

Q9: When is backdrilling useful near a BGA?

A9: It can help when an unused through-via stub affects a bandwidth-sensitive transition. The stack-up, drill access and reliability plan must support it; it is not required for every BGA net.

Q10: What should be sent for a BGA PCB quotation?

A10: Send one revision-controlled package that defines the board, assembly and expected evidence. Include the package information, PCB data, BOM, placement files, quantities, inspection/test requirements and required records.

Conclusion: How Can You Reduce BGA PCB Design Risk Before Production?

BGA risk falls when package, fanout, layer, electrical, thermal and manufacturing decisions are resolved in dependency order. A controlled BGA PCB design process verifies pad and fanout geometry, protects signal and power paths, closes DFM findings and establishes assembly evidence while the footprint, via structure and stack-up can still change.

A free DFM review is available through sales@bestpcbs.com when the package drawing, ball map, native layout or fabrication data, BOM, quantities and inspection/test requirements are ready. EBest Circuit returns the open design inputs, proposed PCB and assembly route, and the evidence to include in the quotation, giving your team a clearer basis for approving the build.

You may also like