PCB manufacturing PCB manufacturing
Home > Blog

AI Server PCB

PCB CCL Shortage 2026: AI Server Demand Tightens Material Supply
Monday, November 9th, 2026

The PCB CCL shortage in 2026 is raising costs and complicating production schedules as AI server demand puts pressure on high-performance laminates. A November supply-chain report shows procurement lead times of 8–10 weeks for several CCL families and 24–32 weeks for selected high-performance materials. Panasonic has announced three rounds of price increases this year, while Kingboard raised prices for certain thin-glass laminates by 15% in October.

Does this mean AI server PCB production will face further delays? Which materials are hardest to source, and how much of the increase will reach finished PCB prices? Recent manufacturer announcements and supplier reports reveal where shortages are occurring, why costs continue to rise, and what engineers and buyers should check before their next production run.
PCB CCL shortage AI server 2026, https://www.bestpcbs.com/blog/2026/11/pcb-ccl-shortage-ai-server-2026/

What Is the Latest PCB CCL Shortage Update in November 2026?

As of November 9, 2026, supply shortages remain concentrated in certain CCL grades and fiberglass constructions rather than the entire laminate market. Availability has become less predictable, particularly for PCB designs requiring specific high-performance materials or thin-glass prepregs.

The clearest evidence comes from a November 4 supply-chain update by VersaLogic. Based on information from one of its PCB suppliers, the company reported CCL procurement periods of approximately 8–10 weeks for several material families, rising to 24–32 weeks for selected higher-performance grades. The supplier also identified shortages of 106, 1080, and 2116 glass fabrics, with multiple CCL manufacturers operating under allocation.

Recent capacity announcements point to the same market pressure. On October 30, Panasonic Industry unveiled a major investment in MEGTRON production, followed by Doosan's November 6 announcement of a new CCL expansion project in China. Both companies are increasing production capacity to support demand from AI infrastructure, although much of the additional output will not become available immediately.

The scale of demand is significant. In May, the Taiwan Printed Circuit Association (TPCA) forecast a US$21.5 billion global CCL market in 2026, up 34.2% year over year. This reflects projected market growth in value, not a measured shortage percentage.

For PCB buyers, the distinction matters. A project may remain on schedule if its approved materials are already available, while another could face delays because a single required laminate or prepreg construction cannot be sourced.

Why Is AI Server Demand Tightening High-Speed CCL Supply?

AI servers require complex multilayer PCBs that consume substantial amounts of specialized materials. As data center investment expands, demand for certain high-performance laminates is growing faster than qualified manufacturing capacity can respond.

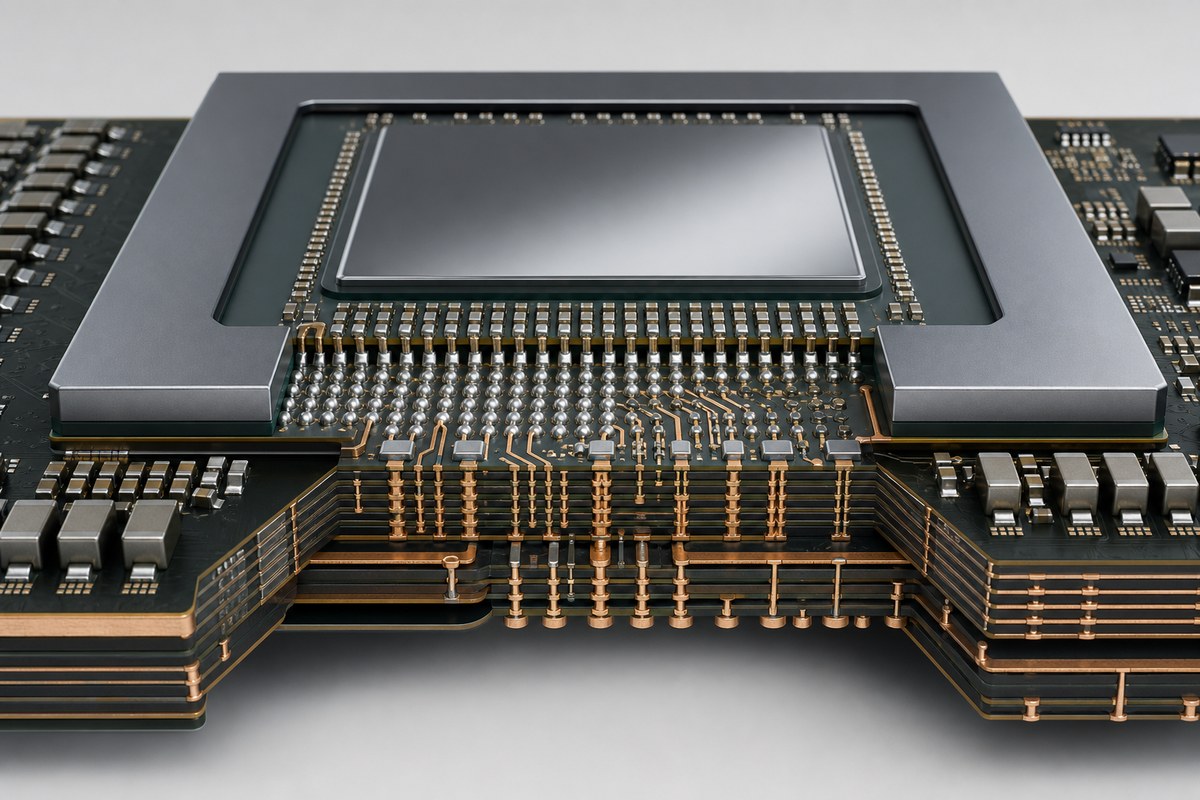
Advanced AI server and networking boards can exceed 40 layers and use large PCB formats. These designs require multiple laminate cores and prepreg layers, often with tightly controlled thickness and electrical specifications. More layers and larger board areas generally increase material consumption, although the actual amount depends on the stackup and panel layout.

High-speed signal requirements further restrict sourcing options. Long electrical channels may require low dielectric loss, controlled dielectric properties, and specific copper foil characteristics. Once a material has been approved for signal integrity and reliability, changing to another grade may require additional engineering evaluation and customer approval.

Upstream manufacturing capacity is another constraint. Certain thin or specialty fiberglass fabrics require dedicated equipment and tightly controlled production processes. Adding CCL production lines cannot immediately increase output if the required glass fabric remains unavailable.

This explains why the shortage extends beyond premium AI server laminates. AI-related demand is not responsible for every supply problem, but competition for upstream fiberglass and other materials can affect conventional multilayer PCBs as well.

Which CCL Materials Are Most Affected by the 2026 Shortage?

The strongest reported supply constraints involve selected high-performance laminate grades and specific fiberglass constructions. There is no evidence that every low-loss laminate or standard FR-4 product is experiencing the same shortage.
PCB CCL shortage AI server 2026, https://www.bestpcbs.com/blog/2026/11/pcb-ccl-shortage-ai-server-2026/

For engineers reviewing PCB stackups, the following distinctions are important.

Material Reported Supply Situation What Buyers Should Verify
Selected high-performance CCL Procurement periods of 24–32 weeks reported by one supplier Exact grade, inventory, allocation
Several other CCL families Procurement periods of 8–10 weeks reported Manufacturer, thickness, delivery date
106, 1080, 2116 glass fabrics Shortages reported within one PCB supplier network Approved prepreg construction
M8/M9-class materials Strong demand; availability differs by grade Specific product and qualification
Conventional FR-4 Selected constructions exposed to glass supply and cost pressure Core and prepreg specifications

The difference between glass fabric and finished laminate is particularly important. The numbers 106, 1080, and 2116 identify glass fabric styles, not complete CCL products. Different resin systems and laminate grades may use these fabrics, so a shortage of one construction does not establish that every related laminate is unavailable.

The same caution applies to M8/M9 terminology. These names are commonly used for high-performance material categories, but actual availability must be checked against a manufacturer's specific product. One approved grade may be available while another faces an extended procurement period.

When checking material availability, provide the manufacturer, laminate grade, core thickness, prepreg construction, copper foil requirements, and order quantity. A general inquiry about high-speed CCL rarely provides enough information for a reliable delivery commitment.

What Are Major CCL Manufacturers Reporting About Supply and Capacity?

Panasonic and Doosan have announced substantial investments in high-performance CCL production, but much of the new capacity will enter operation over the next several years. Their expansion plans suggest continued demand from AI infrastructure while highlighting the time required to increase qualified supply.

Panasonic Industry announced a JPY 92 billion AI-related investment program on October 30, including approximately JPY 67 billion for expanding MEGTRON production in Suzhou, China, and Ayutthaya, Thailand.

The company's Suzhou Phase I facility is scheduled to begin mass production in December 2026, followed by Ayutthaya Phase I in November 2027. Additional expansion phases are planned for August 2028 in Suzhou and April 2029 in Ayutthaya.

Doosan is pursuing a similar expansion strategy. Its KRW 970 billion CCL investment plan, announced in September, includes new production capacity in South Korea and China.

On November 6, Doosan confirmed a KRW 550 billion investment agreement for a new production facility near its existing Changshu plant. The project will be developed in stages, with operations expected to begin progressively in the second half of 2028.

Both manufacturers are targeting materials used in AI accelerators, network switches, optical communication equipment, and other high-performance applications.

These investments may improve supply over time, but new facilities must still complete production ramp-up and any required customer qualification. For buyers planning PCB production in the coming months, confirmed material inventory and supplier allocation remain more important than future capacity announcements.

Why Are CCL Prices Rising in 2026, and What Is the Price Trend?

CCL prices have risen repeatedly in 2026 as manufacturers face higher input costs while demand for selected laminates remains strong. Fiberglass shortages are an important factor, but resin, energy, logistics, and other manufacturing expenses are also contributing.

Kingboard's October price notice illustrates the fiberglass supply problem. The company cited strong demand for thin glass cloth, tight supplies of glass fabric and yarn, and rising upstream costs when announcing a 15% price increase for laminates and prepregs manufactured using 2116 or thinner glass fabrics.

Panasonic's announcements reflect broader cost pressure. Its June notice identified higher costs for petrochemical-derived materials, including resins and solvents, along with international logistics disruptions. Its August notice again pointed to elevated raw material, energy, auxiliary material, and transportation costs.

AI server demand has increased pressure on advanced CCL products, but it would be inaccurate to attribute every material price increase solely to AI infrastructure.

How Have CCL Prices Changed in 2026?

Panasonic announced three separate price adjustments for circuit board materials, taking effect in May, August, and September. Kingboard followed with another adjustment in October.

Effective Date Manufacturer General Multilayer CCL Low-Loss / Other CCL
May 1, 2026 Panasonic +30% MEGTRON/XPEDION +20%
August 1, 2026 Panasonic +20% MEGTRON/XPEDION +10%
September 1, 2026 Panasonic +30% MEGTRON/XPEDION +15%
October 13, 2026 Kingboard +15% for specified thin-glass laminates and prepregs Depends on covered product

These figures represent the manufacturers' announced adjustments for specific materials and pricing periods. They cannot simply be added together to calculate a universal annual CCL price increase. Actual transaction prices depend on the applicable commercial terms.

The announcements nevertheless show that material cost pressure persisted through several pricing rounds during 2026.

How Much Will This Add to Finished PCB Costs?

A 20% increase in a laminate grade does not automatically mean a 20% increase in the finished PCB quotation.

CCL is only one part of total fabrication cost. Drilling, plating, imaging, lamination, inspection, testing, and other manufacturing operations also contribute to the final price.

A high-layer-count AI server PCB containing a large amount of specialized low-loss material may be more exposed to certain price increases than a simpler industrial board. Even two PCBs with the same layer count can be affected differently if their dimensions, material specifications, and panel utilization differ.

When a new quotation is higher, ask which laminate has increased in price, whether the same approved grade is still being quoted, and whether the change reflects current purchasing costs or an existing supply agreement.

That provides a more useful basis for evaluating PCB cost changes than the headline material price increase alone.

How Is the CCL Shortage Affecting AI Server PCB Manufacturing?

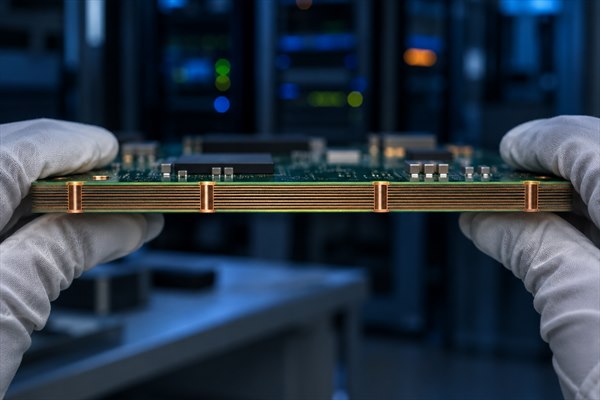
The main manufacturing risk is that one unavailable material can delay an otherwise production-ready multilayer PCB order. This is especially relevant to complex stackups using several different core thicknesses and prepreg constructions.
PCB CCL shortage AI server 2026, https://www.bestpcbs.com/blog/2026/11/pcb-ccl-shortage-ai-server-2026/

Consider a high-layer-count server PCB requiring multiple approved core and prepreg materials. The manufacturer may have sufficient inventory of most materials, but if one specified prepreg cannot be obtained, the approved layup cannot be completed. Production may be delayed before the board reaches the lamination stage.

Order quantity creates another challenge. A PCB manufacturer may have enough approved material to produce 20 prototype boards but insufficient inventory for a follow-on order of 1,000 units.

Successful prototype fabrication therefore does not guarantee that the same material will be available for mass production.

A proposed material replacement may introduce further delays. A different dielectric system can affect finished thickness, impedance, signal loss, lamination behavior, or reliability assumptions. Any necessary engineering review or qualification work must be completed before the revised construction is approved.

This is why PCB delivery schedules should account for both material readiness and available fabrication capacity. A factory may have an open production slot without having every material required to use it.

Can Engineers Replace Short-Supply CCL Materials Without Compromising PCB Performance?

An alternative CCL may be acceptable, but matching the material category or nominal Dk is not enough to establish interchangeability. High-speed PCB performance depends on the complete dielectric and conductor construction.

Panasonic's MEGTRON 8 family provides a useful example.

At 14 GHz, the manufacturer's published typical values for R-579Y(U) are Dk 3.08 and Df 0.0012, compared with Dk 3.13 and Df 0.0016 for R-579Y(N).

These values are typical test results, not guaranteed limits. Although the materials belong to the same family, their electrical properties differ. Whether those differences matter depends on channel length, operating frequency, and the available signal-loss budget.

Before approving a substitute, the engineering review should cover:

  • Electrical properties: Compare Dk and Df at relevant frequencies, then evaluate controlled impedance and channel loss.
  • Stackup construction: Confirm core thickness, cured prepreg thickness, glass style, resin content, and copper foil characteristics.
  • Thermal and mechanical properties: Review Tg, Td, CTE, dimensional stability, and compatibility with the required assembly cycles.
  • Qualification requirements: Determine whether updated simulation, prototype testing, reliability testing, or formal customer approval is required.

The review should use comparable material data and the actual finished stackup. Similar datasheet values alone do not guarantee equivalent PCB performance.

For a design already released to manufacturing, retaining the approved material and adjusting the delivery schedule may sometimes present less risk than introducing an unqualified substitute.

The decision should be based on electrical performance, manufacturing compatibility, and qualification requirements, rather than material availability alone.

What Is the Current Lead Time for High-Speed CCL Materials?

The latest supplier report published on November 4 indicates procurement periods of 8–10 weeks for several CCL families and 24–32 weeks for selected higher-performance materials.

These figures came from one PCB supplier's October update, so they should not be treated as standard lead times for every material or manufacturer.

Actual availability can differ significantly between PCB factories. One manufacturer may already hold enough approved laminate to start production, while another must wait for new material deliveries or allocation confirmation.

Material procurement must also be distinguished from PCB fabrication.

If an approved laminate is already in stock, the normal PCB manufacturing schedule may still be achievable. If the material has not been allocated, even a factory offering quick-turn PCB services cannot guarantee the original shipment date.

When reviewing a quotation, ask for three confirmed dates: material availability, planned production start, and finished PCB shipment.

A single quoted lead time is less useful when material procurement and fabrication depend on different suppliers or unresolved allocations.

How Can PCB Buyers Reduce CCL Supply and Delivery Risks?

The best time to address material shortages is before the PCB order is released, while purchasing requirements and the manufacturing schedule can still be reviewed together.

For AI server and high-speed multilayer PCB projects, buyers should focus on the following checks:

  • Confirm the approved material specification: Identify the exact laminate, core, prepreg, and copper foil requirements. Record any alternatives already approved by engineering.
  • Verify material availability: Ask whether the required quantity is physically in stock, reserved for the order, or awaiting supplier allocation.
  • Check prototype-to-production continuity: If prototypes are being built first, confirm how the same approved material will be secured for volume production.
  • Review purchasing terms: Check quotation validity, material pricing assumptions, order quantities, and conditions governing delivery changes.
  • Control material substitutions: Any proposed replacement should be evaluated against the released PCB specification before manufacturing proceeds.
  • Confirm delivery milestones: Separate material arrival, fabrication, inspection, and shipment dates rather than relying on a generic total lead time.

For repeat orders, sharing a realistic production forecast can help the PCB manufacturer coordinate purchasing arrangements with its material suppliers. However, a forecast does not reserve inventory unless a specific commitment has been agreed.

These checks reduce the risk of discovering a material shortage after a delivery date has already been promised to the end customer.

Will the PCB CCL Shortage Continue Into 2027?

Some CCL supply constraints may continue through 2027, particularly for specialized high-performance grades and fiberglass constructions. However, the market does not have one confirmed recovery date.

VersaLogic's November report included a supplier expectation that tight conditions could persist into 2027 or 2028 while manufacturers expand capacity, introduce new glass-cloth equipment, and complete material qualifications.

That is one supplier's outlook rather than a guaranteed forecast for the entire industry.

The expansion schedules announced by Panasonic and Doosan suggest that additional high-performance CCL production capacity will become available gradually.

Panasonic expects new production milestones in late 2026 and 2027, while significant additional capacity from both companies is scheduled for 2028 and beyond.

The pace of recovery will depend on how quickly new lines reach stable production, whether specialty fiberglass supplies improve, and how much of the additional output is absorbed by AI infrastructure demand.

Standard laminates and advanced low-loss products may recover at different rates.

Buyers planning PCB production in 2027 should therefore monitor approved material grades and actual supplier commitments, rather than assume that broader CCL capacity expansion will resolve every sourcing problem.

FAQs About the 2026 PCB CCL Shortage

Q1: What Is the Difference Between Copper-Clad Laminate and Prepreg?

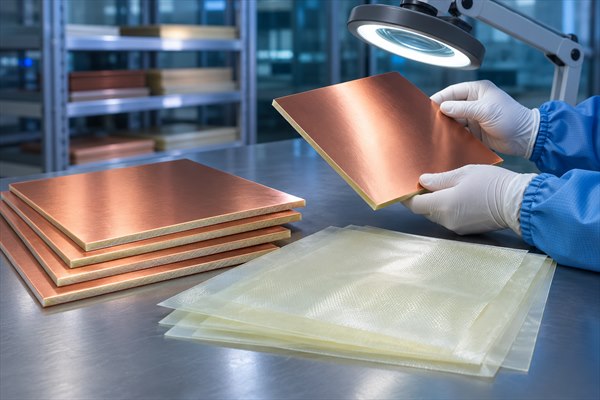
A1: Copper-clad laminate (CCL) consists of a cured insulating substrate bonded to copper foil, while prepreg is resin-impregnated reinforcement that is not yet fully cured. During multilayer PCB lamination, prepreg bonds cores and copper layers together. Both materials are essential to the stackup, but they have different storage, processing, and handling requirements.

Q2: Does FR-4 Refer to a Specific CCL Material Grade?

A2: No. FR-4 is a broad flame-retardant glass-reinforced epoxy material designation, not a single manufacturer's product. Different FR-4 laminates can have different thermal, electrical, and mechanical characteristics. A purchasing specification should identify the appropriate material properties, grade, and applicable standards rather than relying on the FR-4 designation alone.

Q3: Does a 40-Layer PCB Require 40 Separate CCL Sheets?

A3: No. Forty layers generally refers to 40 conductive copper layers, not 40 separate laminate cores. A multilayer PCB is constructed using a combination of copper-clad cores, prepregs, and sometimes copper foils. The number of cores depends on the stackup and fabrication method, so material consumption cannot be determined from layer count alone.

Q4: What Is Fiber-Weave Skew in High-Speed PCBs?

A4: Fiber-weave skew occurs when signals experience different propagation delays because of variations in the glass and resin distribution within the dielectric. It can affect timing relationships in high-speed differential pairs. The significance depends on routing geometry, material construction, and data rate. Material selection and routing strategies can help manage the risk.

Q5: Can CCL and Prepreg Be Stored Indefinitely Before PCB Manufacturing?

A5: No. Prepreg generally has manufacturer-defined storage conditions and a recommended shelf life, while cured CCL has different handling and storage requirements. Temperature, humidity, packaging condition, and material age can affect suitability for processing. Manufacturers should follow the relevant material supplier's instructions and evaluate any material outside its recommended storage conditions before use.

Q6: What Does a CCL Certificate of Conformity Confirm?

A6: A Certificate of Conformity (CoC) generally confirms that supplied material meets the specifications or requirements identified by the issuer. It does not necessarily provide individual measured test results for every material property. Buyers should check the certificate's scope and request additional test or traceability documentation when required by the project.

Q7: Does RoHS Compliance Mean a CCL Material Is Halogen-Free?

A7: No. RoHS compliance and halogen-free requirements are different. RoHS restricts specified hazardous substances in electrical and electronic equipment, while halogen-free material requirements commonly address chlorine and bromine content under applicable specifications. A RoHS-compliant laminate is not automatically halogen-free. Both claims should be verified against the relevant requirements and supporting documentation.

Q8: Are ABF Package Substrates and AI Server PCB Laminates the Same Material?

A8: No. ABF (Ajinomoto Build-up Film) is a dielectric material used in advanced semiconductor packaging substrates, while conventional PCB CCL is typically a copper-clad reinforced laminate. The materials serve different manufacturing and performance requirements. Although both supply chains can be influenced by AI hardware demand, their production capacities and shortage conditions should be evaluated separately.

The PCB CCL shortage in 2026 is being shaped by strong AI server demand, tight supplies of certain fiberglass constructions, and repeated increases in material and manufacturing costs. For PCB engineers, the priority is protecting the approved stackup and electrical performance; for buyers, it is securing material quantities and delivery commitments before production begins.

If you are planning a high-speed, multilayer, or AI server PCB project, EBest Circuit offers PCB fabrication, assembly, and a free DFM check. Send your Gerber files, approved stackup, material specifications, order quantity, required delivery date, and delivery location to sales@bestpcbs.com for a manufacturing review and quotation.
You may also like

UBB PCB (Universal Baseboard): Manufacturing Guide for AI Accelerators
Thursday, August 20th, 2026

A UBB PCB is the large, high-speed Universal Baseboard that connects multiple AI accelerator modules. For AI accelerators, its signal paths, power distribution, connector accuracy, and mechanical fit directly affect whether the system can be assembled and operated reliably. Even if a board passes a basic open/short test, incorrect impedance, voltage drop, connector alignment, or flatness can still cause unstable links, poor contact, overheating, or tray interference.

EBest Circuit (Best Technology) supports complex multilayer and HDI PCB manufacturability review, controlled-impedance fabrication, agreed sourcing and PCBA, inspection, and test coordination from prototype through production. System architecture and final platform validation remain with the customer. Planning a UBB PCB build? Send your stackup, fabrication data, drawings, impedance requirements, quantity, and assembly scope to sales@bestpcbs.com for an engineering and quotation review.

UBB PCB
UBB PCB connecting multiple accelerator module positions on one large baseboard.

What Is a UBB PCB?

A UBB PCB is the Universal Baseboard that carries and connects multiple OAM accelerator modules in an AI computing platform. It acts as the common electrical and mechanical foundation between the accelerator modules and the rest of the system.

Its main roles include:

  • Module connection: provides defined locations and interfaces for OAM modules.
  • High-speed interconnect: carries host and module-to-module data paths.
  • Power distribution: delivers the required power domains to accelerator modules and supporting circuits.
  • Management support: routes clock, reset, monitoring, debug, and other sideband signals.
  • Mechanical integration: aligns the modules with the host interface, power hardware, tray, and cooling system.

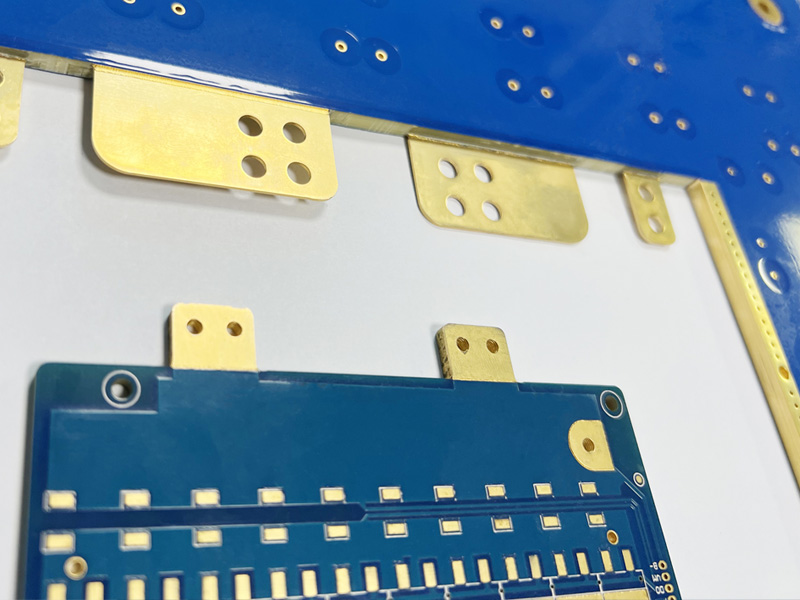
The UBB is not the accelerator module itself. The OAM carries the accelerator device and local circuitry; the UBB connects several modules into one platform. The applicable OCP/OAI revision and final production files determine the actual implementation.
How Does a UBB PCB Connect OAM Modules?

A UBB PCB connects OAM modules through precisely located high-density interfaces. In simple terms, the relationship is: OAM modules → UBB PCB → host, power, and management interfaces. Reliable operation also depends on mechanical compatibility with the tray and cooling hardware.

Four interfaces must agree:

  • OAM-to-UBB: connector footprint, pad geometry, mating height, keep-outs, and module position.
  • UBB-to-host: host-interface lanes, clocks, resets, and other control signals.
  • UBB-to-power system: power connector locations, voltage domains, current paths, and standby rails.
  • UBB-to-chassis: board outline, mounting holes, tray features, cooling clearance, and service access.

A connector can be electrically correct but mechanically unusable if hole locations, flatness, or mating clearance drift. Before fabrication, confirm the OAM, host interface board, power distribution board, tray, and cooling drawings use the same controlled revision.

What Are the Key UBB PCB Specifications?

A UBB PCB does not have one universal layer count, thickness, material, or copper construction. However, UBB designs usually share several manufacturing characteristics because they must connect multiple OAM modules on one large electrical and mechanical platform.

Typical characteristic Why it matters on a UBB PCB
Large format Fits multiple OAM, host, power, and mounting interfaces.
High layer count Provides routing, reference planes, and power layers.
Low-loss construction Supports long accelerator signal paths.
Controlled impedance Preserves critical signal geometry.
Complex vias/backdrill Enables dense routing and limits via stubs.
High-current copper Carries module power through planes and vias.
Mechanical control Maintains flatness, alignment, and module fit.

These are common UBB PCB characteristics, not fixed values. The released platform specification and fabrication package must define the actual board outline, finished thickness, layer construction, materials, copper weights, impedance targets, via structures, backdrill limits, connector requirements, and flatness tolerances.

Why Is UBB PCB Manufacturing So Challenging?

UBB PCB manufacturing is challenging because one large baseboard must support several OAM interfaces, long high-speed channels, high-current structures, and strict module-to-tray alignment at the same time. Each requirement is demanding on its own; their interaction on the same board creates the distinctive UBB manufacturing risk.

The main manufacturing risks are:

  • Multiple OAM interfaces: connector fields must remain aligned with every module position across a large board.
  • Long high-speed channels: material behavior, impedance geometry, vias, and backdrill accuracy accumulate across extended routes.
  • High-current and fine-signal features: heavy power copper and precise signal geometry need compatible lamination, imaging, etching, and plating controls.
  • Large-board flatness: copper imbalance or material movement can affect module seating, connector engagement, and tray installation.
  • Late-stage yield exposure: a hidden lamination, plating, registration, or dimensional defect can scrap the complete multi-module baseboard.

The key difficulty is therefore not simply making a high-layer-count PCB. It is keeping signal, power, and mechanical requirements within tolerance across the entire UBB after repeated lamination, drilling, plating, and thermal processes.

What Stackup and Materials Are Used for UBB PCBs?

A UBB stackup normally has to satisfy three competing requirements: low-loss signal transmission, high-current power distribution, and dimensional stability across a large board. This is why UBB material selection cannot be separated from layer construction, copper balance, via design, and finished thickness.

A practical UBB stackup usually combines:

  • High-speed signal layers: low-loss laminate, controlled dielectric thickness, suitable copper profile, and adjacent reference planes support long accelerator interconnects.
  • Power and ground layers: multiple plane layers and appropriate copper weights distribute module current while providing stable signal return paths.
  • Routing and transition structures: through vias, blind or buried vias, via-in-pad, and backdrilling may be combined where OAM escape density or stub control requires them.
  • Balanced construction: symmetric materials and copper distribution help control bow, twist, thickness, and connector coplanarity on the large baseboard.

Low-loss materials are important because UBB channels can cross a substantial portion of the baseboard and pass through several via or connector transitions. These low-loss materials must also remain compatible with the selected copper, lamination cycle, and mechanical requirements. Heavy copper helps power delivery but can make etching, resin filling, lamination, and warpage control more difficult. The approved production stackup must balance both needs rather than optimizing either one in isolation.
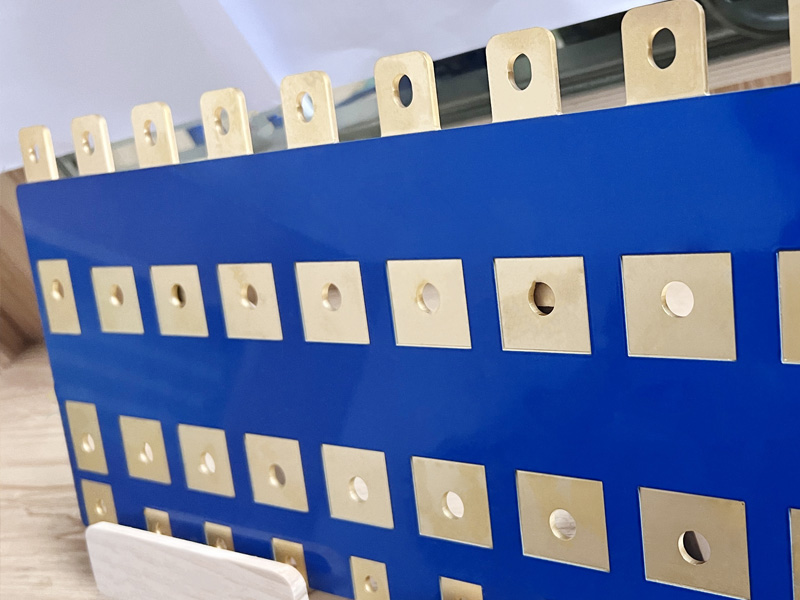
A material brand alone does not define performance. The production stackup should state the actual dielectric system, glass style, copper profile, dielectric thickness, copper weights, impedance geometry, and permitted material alternatives.

UBB PCB
Stackup, material, via, and backdrill review for a complex UBB PCB.

How Does a UBB PCB Handle High-Speed Signals?

A UBB PCB handles high-speed signals by preserving controlled geometry and reference-plane continuity across long routes between multiple module and system interfaces. Because a UBB can combine extended traces with several via and connector transitions, small manufacturing deviations can accumulate into greater channel discontinuity or loss. Manufacturing must therefore reproduce the customer's validated materials, traces, vias, antipads, and residual stubs.

Evidence to request from the PCB manufacturer includes:

  • An approved production stackup with the actual impedance geometry.
  • Controlled differential-pair width, spacing, copper compensation, and reference planes.
  • Backdrill depth and residual-stub control where required by the channel design.
  • Registration checks for connector pads, vias, antipads, and plane clearances.
  • Lot-linked impedance coupons and TDR (time-domain reflectometry) results.

TDR confirms the manufactured impedance structure; it does not prove the complete system channel. The customer validates signal integrity, while the manufacturer provides fabrication records that can be compared with simulation and platform results.

How Does a UBB PCB Handle High-Power Distribution?

A UBB PCB handles high-power distribution by reproducing the customer's defined power paths through power connectors or press-fit interfaces, copper planes, neck-down regions, plated vias, and via arrays. The fabrication task is to preserve the specified copper cross-section and geometry from each power entry to the relevant module interfaces.

The most important PCB manufacturing features are:

  • Copper construction: specified foil and plated copper thickness must be achieved on planes, traces, and finished holes.
  • Plane and neck-down geometry: local restrictions near connectors, cutouts, or dense signal regions must not reduce the intended current path.
  • Via arrays: finished hole size, plating thickness, via count, and spacing determine the available vertical copper cross-section.
  • Power connector holes: drilled diameter, plating, positional tolerance, and press-fit requirements must match the released connector drawing.
  • Heavy-copper lamination: resin filling, copper balance, and material flow must be controlled to avoid voids, thickness variation, and warpage.

These features influence resistance, voltage drop, temperature rise, and mechanical reliability, but the manufacturer does not replace the customer's power-integrity design. EBest reviews whether the released copper, hole, plating, and material requirements are manufacturable and provides the agreed copper records, microsections, dimensional results, or electrical tests for acceptance.

How Should a UBB PCB Be Inspected and Tested?

A UBB PCB should be inspected with a risk-based plan that covers internal circuitry, vias, impedance, dimensions, mechanical fit, and—when assembly is included—hidden solder joints and customer-defined functional checks.

Ask for evidence that answers these customer questions:

  • Was the approved material and stackup used? Review material and stackup records.
  • Were circuit defects detected before lamination or shipment? Review internal and external AOI results.
  • Will the board fit the modules and tray? Check the outline, connectors, mounting holes, thickness, and flatness report.
  • Are hidden vias and backdrills acceptable? Review microsections for plating, resin fill, lamination, and residual stubs.
  • Does the bare board match the netlist? Require 100% continuity and isolation testing.
  • Was controlled impedance achieved? Review lot-linked TDR coupon results.
  • Are hidden assembly joints acceptable? Use AOI or X-ray where the PCBA risk requires it.
  • Does the assembled board meet the agreed function? Use customer-defined fixtures and pass/fail limits.

Decide before ordering which records are required for prototypes and which must accompany every production lot. EBest can coordinate the required inspection records and keep them tied to the correct lot and file revision.
UBB PCB
Dimensional and electrical inspection of a large UBB PCB.

How to Choose a UBB PCB Manufacturer?

Choose a UBB PCB manufacturer by checking whether its real process capability, engineering response, verification evidence, and production controls match your released board—not by accepting a generic multilayer-PCB claim.

Ask four customer-focused questions:

  • Can they build it? Match board size, thickness, materials, HDI/via construction, backdrill, impedance, and power features.
  • Can they explain the risks before quoting? Expect clear questions about stackup, drill pairs, copper balance, tolerances, and substitutions.
  • Can they prove what they inspected? Define electrical test, TDR, microsections, dimensions, AOI/X-ray, and lot records.
  • Can they repeat the process in production? Confirm material continuity, revision control, critical processes, and production inspection.

A representative sourcing problem occurs when a large UBB is quoted only by layer count and quantity. If material construction, board size, backdrill, impedance reporting, and flatness are clarified after the order, the price, lead time, or yield expectation can change. A better supplier resolves these items before the build and records every approved exception.

EBest Circuit can review controlled fabrication data, stackup, drill files, drawings, impedance requirements, quantities, and the agreed PCBA/test scope. Our role is to identify manufacturing gaps early, build to the approved package, and provide the agreed evidence for customer acceptance.

FAQs About UBB PCB

Is a UBB PCB the same as an OAM module?

No. The UBB is the shared baseboard that connects multiple OAM modules. An OAM is the accelerator module installed into the UBB interface.

Does every UBB PCB use the same layer count and material?

No. Stackup, materials, copper, vias, and thickness depend on the platform's signal, power, mechanical, and manufacturing requirements.

Does an OCP UBB specification replace the production files?

No. It provides an architecture and interface reference. Manufacturing still requires final fabrication data, drawings, stackup, drill files, materials, and acceptance criteria.

What should be tested before a UBB PCB is assembled?

Confirm the stackup, dimensions, continuity, isolation, critical vias, impedance, flatness, and connector locations before assembly.

What files should I send for a UBB PCB quotation?

Send the fabrication data, drill files, approved or target stackup, impedance requirements, material notes, mechanical drawings, acceptance criteria, revision, quantities, and—if needed—BOM, placement, assembly, and test files.

Need a UBB PCB manufacturing review? Send your final files, quantities, and PCB/PCBA requirements to sales@bestpcbs.com. EBest Circuit will identify open manufacturing questions and confirm the next steps before production.

You may also like

AI Server PCB Design: Stackup, Signal Integrity and Power Delivery
Thursday, August 13th, 2026

AI server PCB design must coordinate high-speed channels, dense accelerator routing, large transient currents, thermal limits, and manufacturable stackup details from the start. A board can pass ordinary design-rule checks and still fail if its material model, via structure, reference planes, power delivery network, and released fabrication data describe different electrical assumptions.

The practical goal is not to choose the highest layer count or the most expensive laminate. It is to convert the system architecture into a controlled board structure that can be simulated, fabricated, assembled, measured, and revised without losing traceability.

AI Server PCB Design on a high-density accelerator motherboard

What Is AI Server PCB Design?

AI server PCB design is the board-level engineering used for accelerator cards, server motherboards, backplanes, switch boards, power boards, and related high-performance computing hardware. It connects processors, accelerators, memory, storage, network interfaces, power conversion, management controllers, and mechanical interfaces within defined electrical and thermal margins.

The phrase should not be confused with AI-assisted PCB software. Here, “AI” describes the server workload and hardware architecture. The design challenge comes from dense interconnects, high aggregate bandwidth, fast current steps, large packages, and tight airflow or cold-plate constraints.

How Does an AI Server PCB Differ from a Standard Server Board?

An AI server PCB usually concentrates more high-speed lanes and higher power density around accelerators than a general-purpose server board. The exact difference depends on the platform, but the following design domains commonly become more tightly coupled.

Design Domain AI Server PCB Focus Release Evidence
High-speed links Loss, crosstalk, return paths, transitions, and connector channels Channel model, routing rules, and measured validation plan
Power delivery Low impedance across frequency, transient response, and current sharing PDN targets, plane geometry, capacitor strategy, and power test points
Density BGA escape, microvias, via-in-pad, and layer transitions Stackup, drill table, via structure, and fabrication feedback
Thermal and mechanical Package heat, copper distribution, stiffeners, connectors, and cooling interfaces Mechanical model, thermal assumptions, and assembly constraints

Which Board Architecture Should Be Defined First?

The board role must be defined before the stackup because a motherboard, accelerator card, backplane, and power board do not share the same routing or verification priorities. Start by mapping the interfaces, package transitions, connectors, board outline, cooling method, and power entry points.

  • Identify every high-speed interface and its end-to-end channel boundary.
  • Separate on-board routing from connector, cable, package, and mezzanine contributions.
  • Map voltage rails, expected current steps, conversion stages, and return paths.
  • Lock connector zones, keep-outs, fastener locations, stiffeners, and cooling interfaces.
  • Assign owners for SI, PI, thermal, mechanical, PCB, assembly, and validation decisions.

This architecture map prevents a local layout improvement from consuming margin needed elsewhere in the system.

How Should the AI Server PCB Stackup Be Planned?

The stackup should be derived from routing density, reference-plane continuity, impedance structures, power distribution, via transitions, total thickness, and fabricator constraints. There is no universal layer count for an AI server board.

Route critical signals next to continuous reference planes and minimize unnecessary reference changes. Power and ground planes should support the PDN strategy, while dielectric choices and finished copper thickness must match the values used in simulation. A proposed stackup is not controlled until the layout rules, impedance table, drill definitions, and fabrication drawing all describe the same build.

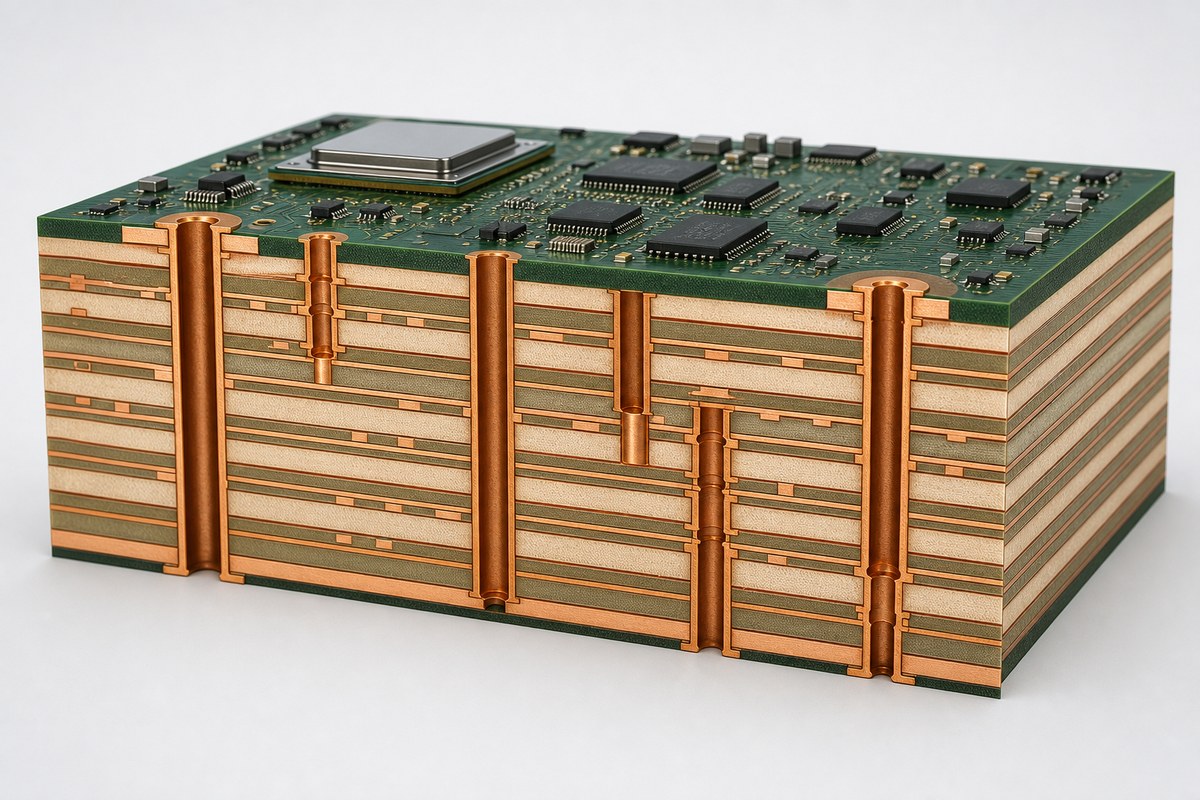
Cutaway of a multilayer AI server PCB stackup with through holes and microvias

For a focused introduction to a related commercial application, see our AI server PCB manufacturing overview.

Which Materials Support High-Speed AI Server Links?

Material selection should follow the channel loss budget, operating frequency range, stackup construction, copper profile, thermal exposure, and supply availability. A laminate name by itself is not an electrical model.

Record the source and test conditions for dielectric constant and dissipation factor. Then align those assumptions with resin content, glass style, finished dielectric thickness, copper roughness, solder mask, and the fabricator’s available constructions. Approving an equivalent material requires more than matching a nominal Dk or Df value; the proposed construction must also preserve impedance, loss, reliability, and manufacturability.

How Should Signal Integrity Be Controlled?

Signal integrity should be controlled as an end-to-end channel, not as isolated trace-width rules. Model the package escape, vias, reference changes, connectors, and routed transmission lines together wherever those transitions consume meaningful margin.

  • Define impedance by routing layer, structure, reference plane, and tolerance.
  • Budget insertion loss, return loss, crosstalk, skew, and discontinuities by interface.
  • Reduce avoidable via stubs and model backdrill or blind-via transitions.
  • Place return vias where a signal changes reference planes.
  • Preserve pair geometry through breakouts, bends, neck-downs, and connectors.
  • Plan coupons, test points, and correlation methods before fabrication release.

Our guides to stripline versus microstrip routing and eye diagram signal integrity explain two parts of this verification path.

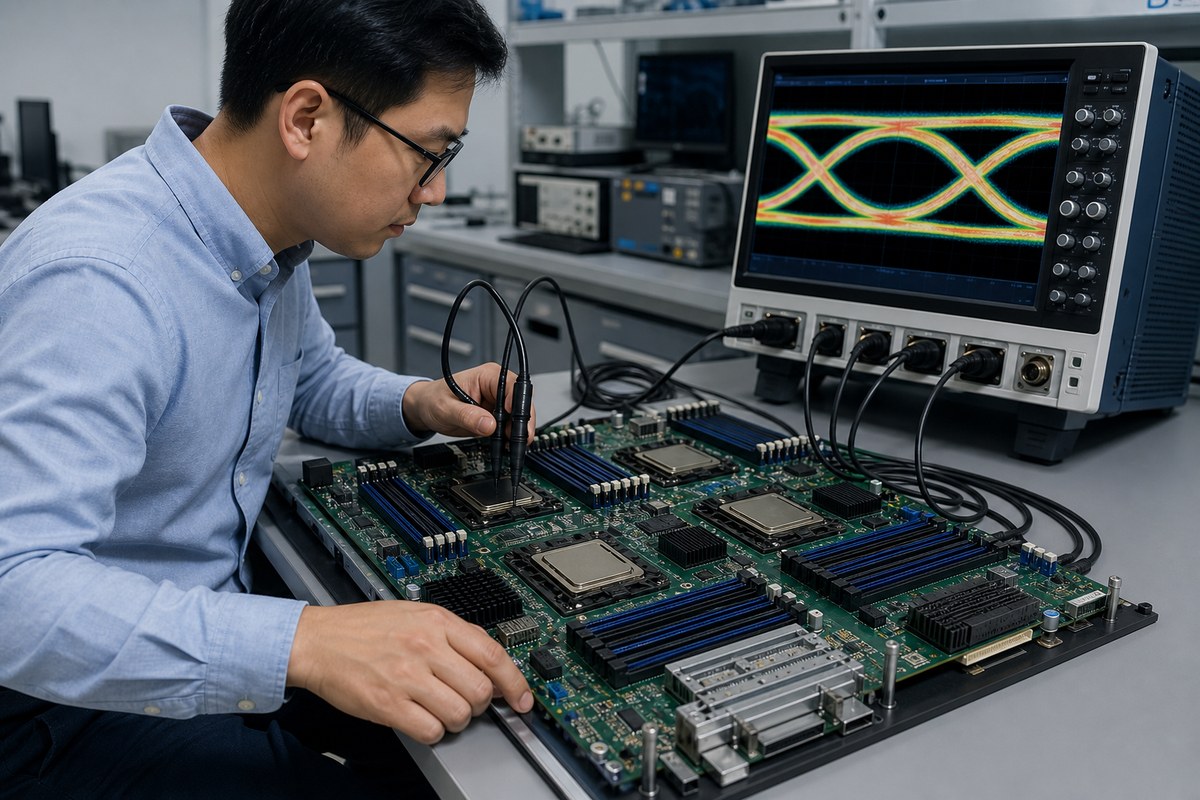
Engineer measuring signal integrity on an AI server PCB with an oscilloscope eye diagram

How Should Power Integrity Be Designed?

Power integrity should keep every critical rail within its allowed voltage window during steady-state and transient operation. The work begins with target impedance and current-step assumptions, then connects regulator placement, plane geometry, decoupling, vias, and measurement access.

Place high-frequency decoupling close to the package power pins through short, low-inductance connections. Use appropriate plane areas and via arrays for current flow, but check the thermal and fabrication consequences of heavy copper concentration. Simulate the PDN over the relevant frequency range and reserve probe access for board-level correlation.

How Should Thermal and Mechanical Constraints Be Coordinated?

Thermal and mechanical decisions must be included before placement is frozen because cooling hardware, board stiffness, package warpage, and connector loading can change the electrical layout. A thermally attractive component location may be poor if it lengthens critical channels or blocks power entry.

  • Coordinate heatsinks, cold plates, airflow, mounting hardware, and keep-outs with placement.
  • Review copper balance, board thickness, panel support, and assembly thermal mass.
  • Protect press-fit zones, edge connectors, and large packages from excessive board flex.
  • Place temperature sensors and validation points where they measure meaningful conditions.
  • Define operating and qualification profiles before selecting materials and assembly cycles.

Which Via Structures Work for Accelerator Escape Routing?

The via structure should solve BGA escape and transition performance without creating an unnecessarily complex build. Through vias remain useful where density and channel performance allow them; blind, buried, and laser-drilled microvias are selected when routing density or stub control requires them.

For an AI accelerator PCB or GPU PCB design, review pad size, capture pad, antipad, aspect ratio, stacked or staggered construction, copper filling, planarization, sequential lamination, and inspection access together. Our microvia aspect ratio guide explains why geometry must be confirmed before release.

AI accelerator BGA escape routing with via-in-pad microvias and multilayer power planes

How Does AI Server PCBA Affect the Layout?

AI server PCBA requirements affect pad design, component spacing, thermal profiling, inspection access, rework strategy, and panel support. Dense BGA packages, heavy copper areas, large connectors, and mixed thermal masses make assembly feedback necessary before the board is finished.

Confirm the package land patterns and paste strategy against component data. Provide access for AOI, X-ray, boundary scan, programming, and functional test where applicable. If a critical BGA cannot be visually inspected, define the X-ray acceptance and process-control approach before production.

What Should Be Verified Before Prototype Release?

Prototype release should occur only after the electrical intent and manufacturing package agree. A file-count checklist is not enough; the review must find contradictions between files and assumptions.

  1. Confirm the board role, interface list, channel boundaries, power rails, and acceptance owners.
  2. Reconcile the stackup, impedance table, routing rules, material model, and total thickness.
  3. Compare every via depth pair and backdrill definition with the actual layer map.
  4. Review SI, PI, thermal, and mechanical assumptions against the released layout revision.
  5. Check Gerber, ODB++ or IPC-2581 data, drill files, fabrication notes, BOM, and placement data for revision consistency.
  6. Define coupons, measurements, test conditions, sample quantities, and pass/fail ownership.
  7. Record approved deviations and decide which changes require re-simulation or requalification.

Use the final URL for this AI server PCB design guide in project documentation so design, manufacturing, and validation teams reference the same release checklist.

FAQ About AI Server PCB Design

How many layers does an AI server PCB need?

There is no fixed layer count. The required stackup follows routing density, reference-plane needs, power distribution, board thickness, connector constraints, and the chosen via architecture. Select the layer count after preliminary placement, escape analysis, channel planning, and fabricator review.

Does every AI server PCB require HDI?

No. HDI is used when package escape, routing density, or transition performance cannot be achieved efficiently with conventional structures. Some support or power boards may not need microvias, while accelerator and dense compute boards often require more advanced interconnects.

Can standard FR-4 be used for AI server PCB design?

It may be suitable for slower support circuits or short channels, but critical high-speed links need a material decision based on the channel loss budget and construction. Do not approve a material from its generic family name alone.

Why is copper roughness important?

Copper surface profile contributes to conductor loss at high frequencies. The simulation model and fabrication specification should use compatible roughness assumptions, especially on long or margin-sensitive channels.

When is backdrilling required?

Backdrilling is considered when unused plated-through-hole stubs consume too much channel margin. The need and residual-stub target should come from transition modeling and must be translated into an unambiguous controlled-depth drill definition.

What is the most important PDN input?

The PDN needs credible rail tolerances, current demand, and transient assumptions. Without them, a target-impedance result may look precise but cannot prove that the processor or accelerator stays within its allowed voltage window.

How early should the PCB manufacturer review the stackup?

Review should start before routing rules and via structures are frozen. Early feedback can align available materials, finished dielectric thicknesses, copper weights, drill structures, and impedance geometries with the design model.

What test structures should be planned?

Plan structures that support the actual acceptance method, such as impedance coupons, loss or correlation structures, power test points, and assembly inspection access. Their design and location should be agreed before panelization.

What files should accompany an AI server PCB RFQ?

Provide the fabrication data, stackup, drill and backdrill definitions, impedance requirements, material assumptions, fabrication drawing, quantities, and revision. For assembly, add the BOM, centroid data, assembly drawings, test requirements, and any programming files.

How can prototype results be carried into mass production?

Keep the material construction, drill structure, process notes, test method, and acceptance evidence under revision control. If a production change alters an electrical or mechanical assumption, route it through the same owners who approved the prototype baseline.

How Can EBest Circuit Support Your AI Server PCB Project?

At EBest Circuit, we support PCB design, prototyping, fabrication, component sourcing, and PCB assembly from the same controlled data package. Our engineering review can help identify conflicts among the stackup, impedance requirements, drill structure, materials, assembly constraints, and released files before the order moves forward.

Send your Gerber or ODB++ data, stackup, drill files, impedance targets, BOM, quantities, and test requirements to sales@bestpcbs.com. Our engineering team can review the package and confirm the applicable manufacturing path for your project.

You may also like

Best AI Server PCB Manufacturer From Design to Assembly
Tuesday, August 11th, 2026

An AI Server PCB project succeeds when its electrical and mechanical requirements survive every handoff from architecture and layout to fabrication, assembly, and testing. The central task is to preserve signal, power, thermal, and mechanical margin in a construction that can be manufactured repeatedly.

Before layout begins, define the board’s role, interface generations, power profile, cooling conditions, connector locations, mechanical limits, and acceptance tests. These inputs determine the materials, stackup, via structure, manufacturing controls, and quotation scope.

AI Server PCB manufacturing review on a large server-class circuit board

What Is an AI Server PCB?

An AI server PCB is a circuit board that carries one or more compute, memory, networking, storage, control, or power functions inside an AI server. Fast interfaces, concentrated power, dense packages, large board formats, and continuous workloads make these boards more demanding than their basic copper-and-dielectric construction suggests.

The term can refer to a host motherboard, accelerator baseboard, network switch board, power distribution board, backplane, or management board. Requirements depend on the processors, interfaces, power rails, connectors, and cooling conditions assigned to that board. Defining its role gives the designer and manufacturer a sound basis for the stackup, materials, via structure, and test plan.

Which PCB Boards Are Used in an AI Server?

An AI server normally uses several PCB boards to perform different system functions. The exact combination depends on the server architecture; common board types are listed below.

PCB Board Primary Function
Host motherboard Connects the CPU, memory, storage, management controller, and expansion devices
Accelerator baseboard Connects GPUs or other accelerator modules and supports communication between them
Network or switch board Transfers data between accelerators, servers, and external networks
Power distribution board Distributes or converts power for processors, accelerators, and other server loads
Backplane Connects multiple server boards, storage devices, or modules through a shared interface
Riser board Changes the orientation or position of expansion cards within the server chassis
Management board Monitors server status and supports remote control, diagnostics, and system management
Storage board Connects and controls SSDs, hard drives, or other storage devices

Not every AI server uses every board listed above. Some functions may be combined on one PCB, while modular platforms may separate them across several boards. Identifying the board type and its function prevents a host motherboard, accelerator baseboard, backplane, or power board from being quoted as though they were the same product.

How Is an AI Server PCB Different from a Standard Server PCB?

An AI server PCB differs from a standard server PCB mainly in accelerator connectivity, local power demand, routing density, cooling loads, and the validation needed to prove stable operation. The exact difference depends on the server architecture, but the board-level comparison below shows the usual design shift.

Comparison Area Standard Server PCB AI Server PCB
Board architecture Primarily connects CPUs, memory, storage, management, and network interfaces Adds dense GPU or accelerator modules and the high-bandwidth fabric that connects them
High-speed routing Channel count and routing density follow conventional server interfaces More simultaneous accelerator and fabric links increase breakout, reference-plane, via-transition, and crosstalk constraints
Power delivery Power planes and regulators support conventional processor, memory, storage, and network loads Higher localized current and faster load changes near accelerators demand lower-impedance power paths, stronger decoupling, and closer thermal review
Materials and stackup High-Tg FR-4 or other materials may be sufficient when the verified channel budget allows Long or fast accelerator links may require lower-loss laminate, tighter impedance control, shorter stubs, and additional routing or power-distribution layers
Thermal and mechanical design Board support and cooling are sized for the standard component and heat-sink arrangement Large packages, heavier cooling hardware, concentrated heat, and connector density increase the need to control board support, airflow, bow, twist, and mating alignment
Validation scope Bare-board, assembly, functional, and platform tests confirm the specified server design Validation must also correlate channel margin, power behavior, temperature, mechanical fit, and workload stability across the accelerator platform

A standard server stackup should therefore be reused only after its channel loss, reference planes, power distribution, via structure, board support, and thermal margin have been checked against the AI server architecture.

Why Does an AI Server PCB Need High-Speed and High-Power Design?

An AI server PCB needs high-speed design to move large amounts of data between processors, memory, accelerators, storage, and network interfaces, and it needs high-power design to deliver stable current to those devices under rapidly changing workloads. If either side is inadequate, the server may lose interface margin, suffer voltage instability, overheat, or throttle before it reaches its intended performance.

High-speed design protects signal integrity. Package escape, trace geometry, dielectric loss, copper roughness, vias, reference-plane transitions, connectors, and module interfaces all contribute to channel loss and reflections. The PCB therefore needs controlled impedance, continuous return paths, appropriate materials, and transition structures that keep the complete channel within its electrical budget.

High-power design protects power integrity and temperature margin. Accelerators can draw high local current and change load quickly, so power planes, copper distribution, vias, voltage regulators, and decoupling must limit voltage drop and transient noise while carrying current without excessive heating.

The two requirements must be reviewed together. Dense signal routing can reduce the space available for power copper, while plane splits, large via fields, and copper imbalance can affect return paths, lamination, and thermal behavior. The design target is sufficient signal and power margin under the intended workload and operating temperature—not maximum performance in only one domain.

How Should an AI Server PCB Be Designed?

An AI server PCB should be designed in a controlled sequence from system requirements to a verified production package. Signal, power, thermal, mechanical, manufacturing, and test decisions must be developed together because a change in one area can reduce margin in another.

  1. Define the board role: Identify whether the PCB is a host motherboard, accelerator baseboard, network board, power board, backplane, riser, management board, or storage board, then define its interfaces with the rest of the server.
  2. Set measurable constraints: Record interface generations and channel budgets, rail voltages and current profiles, board outline, connector locations, component heights, cooling zones, mounting points, and required validation results.
  3. Select materials and stackup: Choose laminates, copper weights, layer functions, reference planes, impedance structures, and via types that meet electrical and reliability needs while remaining manufacturable.
  4. Place critical components: Position processors, accelerators, memory, regulators, clocks, connectors, and decoupling parts to shorten sensitive paths, support airflow, and leave realistic breakout and assembly space.
  5. Design the power distribution network: Size planes, pours, vias, regulator connections, and decoupling for DC voltage drop, transient response, current density, and temperature rise at the expected workload.
  6. Route high-speed interfaces: Maintain controlled impedance and continuous return paths, limit discontinuities and stubs, manage lane spacing and length requirements, and review packages, vias, connectors, and cables as one channel.
  7. Review thermal, mechanical, and DFM risks: Check copper balance, heat-sink and board-support loads, airflow, warpage, connector alignment, drill and registration limits, assembly access, and test-point availability.
  8. Verify and release the design: Close signal, power, thermal, mechanical, DFM, and test findings, then issue one synchronized revision of the fabrication data, drawings, stackup, netlist, BOM, assembly files, and acceptance criteria.

Which Materials and Stackups Are Suitable for an AI Server PCB?

AI server PCBs typically use high-Tg FR-4, mid-loss laminate, or low-loss high-speed laminate, selected according to the function and channel budget of each board. Accelerator baseboards and network or switch boards usually need the lowest-loss construction. Host motherboards often combine high-speed routing with substantial power distribution. Management and lower-speed storage boards may use high-Tg FR-4 when verified channel loss remains within the interface budget.

AI Server PCB Type Suitable Material Direction Stackup Priorities
Accelerator baseboard Low-loss laminate with controlled dielectric properties and low-profile copper for long, fast processor-to-processor or processor-to-module links Critical signal layers beside continuous ground references, short via transitions, sufficient power and ground planes, and balanced copper distribution
Network or switch board Low-loss high-speed laminate selected from the total connector, via, and trace loss budget Closely referenced differential-pair layers, controlled breakout and backdrill structures, isolation between channel groups, and stable return paths through connectors
Host motherboard Mid-loss or low-loss laminate for high-speed regions, with high-Tg and reliability characteristics suitable for the complete board Separate routing, reference, and power-distribution functions; enough breakout layers for dense packages; and plane pairs positioned to support return current and decoupling
Power distribution board High-Tg laminate with copper thickness and thermal behavior matched to the required current; low-loss dielectric is usually not the primary need Wide copper areas, parallel power and ground paths, adequate via arrays, thermal balance, insulation spacing, and mechanical support for high-current connections
Backplane or riser Mid-loss or low-loss laminate when it carries high-speed fabrics; high-Tg FR-4 may suit lower-speed control or power-only connections Connector-launch control, continuous references, short transitions, mechanical thickness control, and balanced construction for mating alignment
Management or storage board High-Tg FR-4 for moderate-speed functions, upgraded to a mid-loss material when interface length and speed require more channel margin A simpler multilayer stackup with clear signal references, practical power planes, manufacturable vias, and enough test access

The layer count should not be chosen from the term “AI server” alone. It is determined by package escape, routing density, reference-plane continuity, current distribution, board thickness, via aspect ratio, and mechanical balance. Adding layers without assigning each one a necessary function increases cost and fabrication difficulty without guaranteeing better electrical performance.

Final material approval should be based on the complete channel and construction. Confirm dielectric data at the relevant frequency, copper profile, glass style, resin system, thermal expansion, CAF resistance, availability, pressed thickness, impedance geometry, and fabricator capability. If two laminate families are combined, their bonding, drilling, registration, and thermal compatibility must be reviewed before release.

What Should Be Checked During an AI Server PCB DFM Review?

An AI server PCB DFM review should check the stackup, via architecture, registration margin, copper balance, assembly geometry, and test access against both factory capability and the board’s electrical and mechanical intent. A minimum trace-and-space check alone cannot reveal whether the complete construction is manufacturable.

  • Stackup definition: Confirm material designations, pressed dielectric thicknesses, copper weights, impedance structures, finished board thickness, and permitted material alternatives. The fabrication drawing, impedance table, and layer data must describe the same construction.
  • Via architecture: Review drill sizes, finished hole sizes, aspect ratios, annular rings, capture pads, drill-to-copper clearances, laser-via cycles, buried vias, and backdrill depths as one interconnection system.
  • Registration margin: Check that fine-pitch escapes, dense via fields, plane clearances, and backdrill targets retain enough tolerance for imaging, lamination, and drilling variation.
  • Impedance and return paths: Match the proposed trace geometries to the approved stackup and confirm that reference planes remain continuous through layer changes, connector launches, and high-density breakout regions.
  • Copper and mechanical balance: Review local copper density, plane distribution, board thickness, panel orientation, heavy components, and heat-sink loads to reduce plating variation, bow, twist, and assembly distortion.
  • Assembly geometry: Verify pad and solder-mask geometry, component spacing, polarity markings, stencil-sensitive packages, board support, inspection visibility, and rework access against the intended assembly process.
  • Test access: Reserve usable access for bare-board electrical test, impedance coupons, programming, boundary scan, functional fixtures, and measurement points required by the acceptance plan.

The DFM report should separate mandatory corrections from optional improvements and accepted exceptions. Any proposal that changes impedance, current capacity, timing, thermal paths, component fit, or connector alignment requires documented design approval before fabrication data is released.

How Does AI Server PCB Prototyping Reduce Production Risk?

AI server PCB prototyping reduces production risk by testing the assumptions that control yield, performance, assembly, and system fit before they are repeated across a production lot. A useful prototype build supports six release decisions.

  1. Verify the PCB construction: Measure finished thickness, impedance coupons, microsections, annular rings, backdrill results, bow and twist, and electrical continuity. Use the results to confirm or correct the stackup, drill structure, plating requirements, impedance geometry, and panel process.
  2. Validate high-speed channels: Review link training, eye or margin results, error behavior, and measurements across traces, vias, and connectors. Release the channel only when routing, reference transitions, via stubs, connector launches, and material loss provide sufficient margin.
  3. Prove power delivery: Measure rail sequence, voltage drop, ripple, transient response, current sharing, and temperature at the expected load. Adjust planes, via arrays, decoupling, regulator settings, copper distribution, or cooling where limits are missed.
  4. Check mechanical and thermal fit: Inspect connector alignment, module seating, heat-sink contact, board support, airflow clearance, and operating temperature. Correct the outline, mounting, stiffening, connector position, cooling interface, or chassis tolerance before production.
  5. Qualify the assembly process: Review the first article, AOI, X-ray, solder joints, component coplanarity, and measured reflow profile. Refine stencil apertures, paste volume, support tooling, placement, reflow settings, inspection scope, or rework access as required.
  6. Confirm test and traceability: Verify fixture access, programming, functional logs, serial and lot records, BOM revision, and failure disposition. Finalize test coverage, acceptance limits, fixture controls, data retention, and repeat-order records before release.

Production release requires every prototype finding to have a recorded disposition. The issue must be corrected and retested, accepted with a documented limit, or transferred into a controlled production inspection or test. This prevents an unresolved prototype anomaly from becoming a repeated lot-level failure.

How Is an AI Server PCB Manufactured?

An AI server PCB is manufactured by building and inspecting its inner layers, laminating them into a multilayer panel, forming plated interconnections, completing the outer surfaces, and verifying the finished bare board against the released data. Controls are applied at each stage because buried defects cannot be corrected after the structure is complete.

  1. Engineering and CAM review: Reconcile artwork, netlist, drawings, stackup, controlled-impedance features, drill data, materials, tolerances, and revision identifiers before panelization.
  2. Material preparation: Verify cores, prepregs, and copper foils, then clean and prepare them according to the approved stackup and material-lot controls.
  3. Inner-layer formation: Image, develop, etch, and strip the internal circuitry, then use AOI to find opens, shorts, neck-down, and pattern defects before the layers are buried.
  4. Layup and lamination: Align the inspected cores with prepregs and copper foils, then press the panel while controlling registration, resin flow, pressure, temperature, and finished thickness.
  5. Drilling and hole preparation: Drill plated through-holes and backdrill features as specified, laser-drill microvias where required, then remove resin smear and condition the hole walls. Buried vias are formed within their designated subassemblies before final lamination.
  6. Copper deposition and plating: Deposit conductive copper in the holes and plate them to the specified thickness. Sequential build-up boards repeat imaging, lamination, drilling, and plating for each defined cycle.
  7. Outer-layer formation: Apply the outer-layer image, plate the required copper and etch resist, remove unwanted copper, and inspect the completed external circuitry.
  8. Solder mask and surface finish: Apply and cure solder mask with controlled registration, add permitted markings, and form the specified finish on exposed pads.
  9. Profiling and cleaning: Route, score, or otherwise form the final board and panel features, then remove process residues and verify critical dimensions and connector features.
  10. Final bare-board verification: Perform electrical test, dimensional and visual inspection, impedance testing, and any specified microsection or construction checks before final identification, packaging, and release.

Traceability should connect the finished AI Server PCB to its revision, material lots, process route, approved deviations, and test records. These records establish the manufacturing baseline for repeat orders and failure investigation.

What Does AI Server PCB Assembly Require?

AI server PCB assembly requires accurate component data, controlled material handling, stable board support, package-specific soldering, a measured thermal profile, and first-article approval. The assembly process should be defined around the actual board and component mix rather than a generic SMT recipe.

AI Server PCB assembly on an automated inspection conveyor
  1. Release one consistent assembly package: Align the BOM, manufacturer part numbers, centroid data, assembly drawings, polarity marks, approved substitutions, and PCB revision before components are issued to production.
  2. Control component condition: Verify packaging, lot identification, moisture sensitivity, floor life, baking requirements, solderability risk, and quantities for factory-sourced and customer-supplied parts.
  3. Support the PCB during processing: Use suitable carriers, rails, or fixtures for large, heavy, thin, or densely populated boards so that printing, placement, reflow, and handling do not introduce excessive flex or warpage.
  4. Match solder paste to the package mix: Set stencil thickness, aperture design, paste type, and print parameters for fine-pitch devices, large thermal pads, connectors, BGAs, and components with different solder-volume needs.
  5. Control placement and special assembly steps: Confirm feeder setup, package orientation, placement force, connector seating, press-fit operations, through-hole insertion, hand soldering, and any required heat-sink or hardware installation.
  6. Develop a measured thermal profile: Attach thermocouples to representative high-mass and temperature-sensitive locations, then set preheat, soak, peak temperature, time above liquidus, and cooling conditions for the populated board.
  7. Approve the first article before continuing: Verify component identity, orientation, placement, solder joints, mechanical fit, and required rework on the first completed unit before releasing the remaining build quantity.

How Is AI Server PCB Quality Inspected and Tested?

AI server PCB quality is inspected throughout fabrication and assembly, then verified through electrical and functional testing before release. Each stage targets defects that may become hidden or more expensive to correct later.

AI Server PCB quality inspection with X-ray and optical equipment
  1. Verify materials and production data: Match laminate, prepreg, copper, surface finish, stackup, drill files, netlist, impedance requirements, and revision identifiers to the released order before fabrication begins.
  2. Inspect inner layers before lamination: Use AOI and dimensional checks to detect opens, shorts, conductor damage, incorrect clearances, and registration problems while the circuitry is still accessible.
  3. Control lamination, drilling, and plating: Monitor pressed thickness, layer alignment, hole position, desmear, copper deposition, and plating. Microsections can verify hole-wall copper, interconnection quality, dielectric thickness, and backdrill results where specified.
  4. Test the finished bare board: Perform electrical testing against the supplied netlist, inspect dimensions and workmanship, and verify controlled impedance with the agreed coupons. Additional checks may cover bow and twist, solder-mask registration, surface finish, and final hole size.
  5. Inspect the assembled PCB: Confirm the first article against the BOM, placement data, drawings, polarity, and component orientation. SPI checks solder-paste deposition, AOI examines visible placement and solder features, and X-ray evaluates hidden joints beneath packages.
  6. Run electrical and functional tests: Apply the approved procedure for continuity, shorts, rail sequence, voltage limits, programming, communications, interfaces, and board functions. Each test needs defined limits, recorded results, and a disposition for failures.
  7. Review records before release: Link the shipped boards to their revision, material and component lots, inspection results, test logs, repairs, and approved deviations. Release only units that meet the agreed acceptance criteria.

Factory testing verifies the PCB and assembled board within the agreed test scope; it does not automatically qualify the complete AI server. Firmware, cooling, chassis interaction, workload stability, and full-system performance require validation in the customer’s final platform.

Why Choose EBest Circuit as Your AI Server PCB Manufacturer?

One source from design support to assembled production. EBest Circuit combines PCB design, prototyping, production, component sourcing, and assembly.

  • One accountable supplier: Customers coordinate design support, PCB fabrication, component sourcing, assembly, and production questions through one company instead of managing several disconnected vendors.
  • Lower prototype-transfer risk: EBest supports both prototypes and mass production, allowing approved stackups, revisions, BOM decisions, and inspection requirements to carry into repeat builds.
  • Better technology fit: Available capabilities include multilayer, high-Tg, high-speed, impedance-controlled, HDI, and heavy-copper PCBs for different signal, power, density, and thermal requirements.
  • Earlier engineering review: PCB design support and fabrication are coordinated so that material, stackup, via, impedance, and manufacturability issues can be addressed before release.
  • Simpler component coordination: EBest combines component sourcing with PCB assembly, helping customers manage approved parts, substitutions, consigned components, and shortages within the same project.
  • Documented quality qualifications: EBest’s qualifications include ISO 9001:2015, ISO 13485:2016, IATF 16949, AS9100D, UL, RoHS, and REACH; customers can confirm the scope required for their order.
  • Long-term manufacturing support: Established in 2006, EBest supports custom PCB projects and offers expedited service when the selected materials, processes, components, and inspection requirements allow it.

What Files Are Needed for an AI Server PCB Quotation?

For an accurate AI server PCB quotation, provide five groups of information. Complete inputs prevent conflicting assumptions about fabrication, assembly, testing, and delivery.

  • PCB files: Gerber, ODB++, or IPC-2581 data, plus NC drill files, netlist, board outline, and fabrication drawing.
  • Build requirements: Stackup, materials, copper weights, finished thickness, impedance, via structure, surface finish, tolerances, and acceptance standard.
  • Assembly files: BOM with manufacturer part numbers, centroid data, assembly drawings, polarity information, and special handling notes.
  • Test scope: Required bare-board tests, impedance coupons, programming, functional procedure, acceptance limits, fixtures, and reports.
  • Order details: Prototype and production quantities, requested delivery date, consigned parts, approved substitutions, packaging, and destination.

Use the same revision identifier across every file and clearly mark any requirement that is still undecided.

FAQs About AI Server PCBs

Q1: Is there a fixed minimum order quantity for an AI server PCB?

A1: The practical minimum depends on the board and service scope. The manufacturer should review board size, material, panel utilization, tooling, component packaging, and assembly setup before confirming the smallest workable quantity.

Q2: Can customer-supplied components be used for assembly?

A2: Consigned components can be evaluated. Define quantities, packaging, moisture condition, traceability, incoming inspection, shortages, and replacement responsibility before the build.

Q3: When does the manufacturing lead time begin?

A3: Manufacturing lead time normally begins after order confirmation and engineering release. Unresolved technical questions, incomplete files, unavailable materials, or BOM shortages can delay the production start.

Q4: What happens to unused customer-supplied components?

A4: The disposition should be agreed before assembly. Remaining parts may be returned, stored for repeat orders, or shipped with the finished boards, with quantities and packaging recorded.

Q5: How should long-lead components be managed?

A5: Identify long-lead parts during BOM review. Confirm authorized sources, realistic availability, approved alternatives, and consigned supply before committing the assembly schedule.

Q6: How can sensitive design files be controlled across suppliers?

A6: File access can be limited by responsibility. Each party still needs sufficient controlled data, with revision, transfer, retention, and deletion requirements agreed in advance.

Q7: What happens when a component changes during the product lifecycle?

A7: The change must pass an impact review. Check form, fit, function, layout, firmware, sourcing, manufacturing, and validation before approving the new part.

Q8: Can spare boards be packed for service inventory?

A8: Service stock can use order-specific packaging. Define moisture and ESD protection, labels, serial numbers, accessories, storage conditions, and shipment grouping.

Q9: Who owns the functional test fixture?

A9: Ownership depends on the commercial agreement. Specify design approval, validation, calibration, maintenance, storage, access, modification, and return terms before purchase.

Q10: How are engineering changes handled after an order is placed?

A10: Production data should change only through documented revision control. The manufacturer should confirm affected materials, tooling, work in progress, components, tests, schedule, and approval before implementing the change.

Conclusion

A dependable AI server PCB begins with clear system responsibilities and ends with evidence that the released design can be built, assembled, and verified repeatedly. Define board roles first, convert interface and power needs into a manufacturable construction, use prototypes to close the highest risks, and keep every decision tied to one revision.

Start your AI server PCB quotation today. Send your PCB files, BOM, quantities, and test requirements to sales@bestpcbs.com. EBest Circuit will review the project scope and help move your design toward a controlled prototype or production build.

You may also like