PCB manufacturing PCB manufacturing
Home > Blog

qfn package soldering

Quad Flat No Leads Package: Structure and PCB Assembly
Wednesday, October 7th, 2026

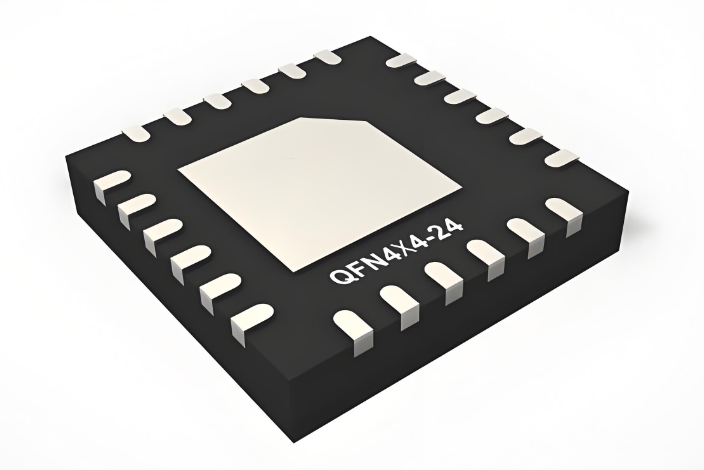
A quad flat no leads package, usually called QFN, is a surface-mount IC package with flat metal terminals along the four edges of its underside. Unlike a QFP, it has no projecting gull-wing leads. Many QFNs also expose a central metal pad that transfers heat into the PCB and may provide an electrical connection. The short connections save space, but most solder joints sit beneath the component. Reliable assembly therefore starts with the exact package drawing—not simply a label such as “QFN-16”—and a matching copper, solder-mask and stencil design.

This article follows the connection from silicon die to PCB, showing how the package structure affects layout and assembly. At EBest Circuit, we support PCB fabrication, component sourcing and PCB assembly. For a QFN-based design, we can review the fabrication and assembly files with your component requirements before production.
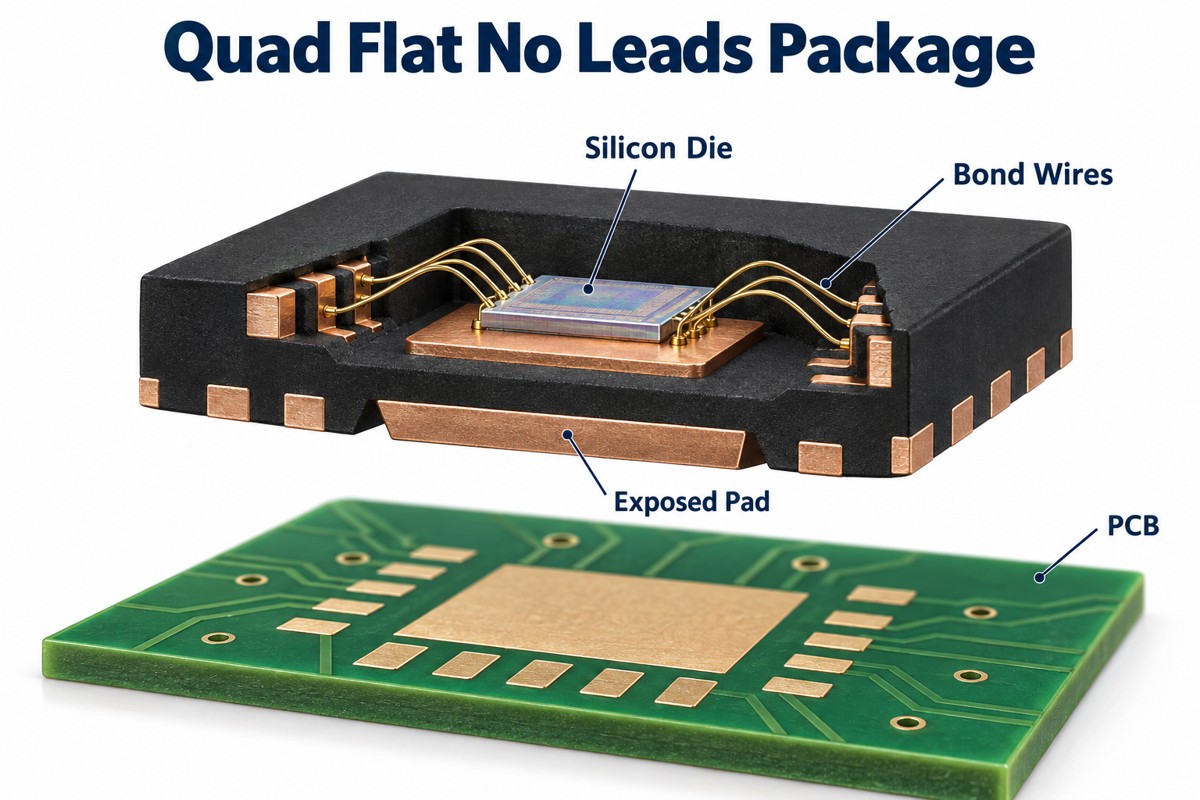
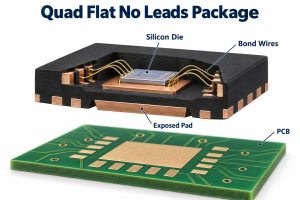
Cutaway of a wire-bonded QFN showing silicon die, bond wires, exposed pad and PCB

Key Takeaways

  • No-lead does not mean no terminals: QFN contacts are flat rather than projecting beyond the body.
  • Wire-bonded and flip-chip QFNs use different internal connections; both can connect to the PCB through bottom terminals.
  • The TI TPS62130 provides a concrete example: a 16-terminal, nominal 3 × 3 mm VQFN with 0.5 mm pitch.
  • The exposed pad has a device-specific electrical function. Its net connection must come from the datasheet.
  • Package dimensions, PCB copper lands and stencil apertures describe three different geometries.
  • Segmented paste openings control solder volume. Paste coverage is not the same measurement as post-reflow voiding.
  • Wettable flanks improve optical access to perimeter fillets; hidden center-pad solder still needs an appropriate inspection plan.

What Is a Quad Flat No Leads Package?

A quad flat no leads package is a low-profile IC housing whose four-sided bottom terminals solder directly to PCB lands. “Quad” refers to the four terminal-bearing sides; “no leads” describes the absence of long external leads.

The name does not identify the circuit inside. A QFN may contain a voltage regulator, interface IC, sensor or controller. Nor does “no-lead” certify lead-free chemistry: package construction and material compliance are separate specifications.

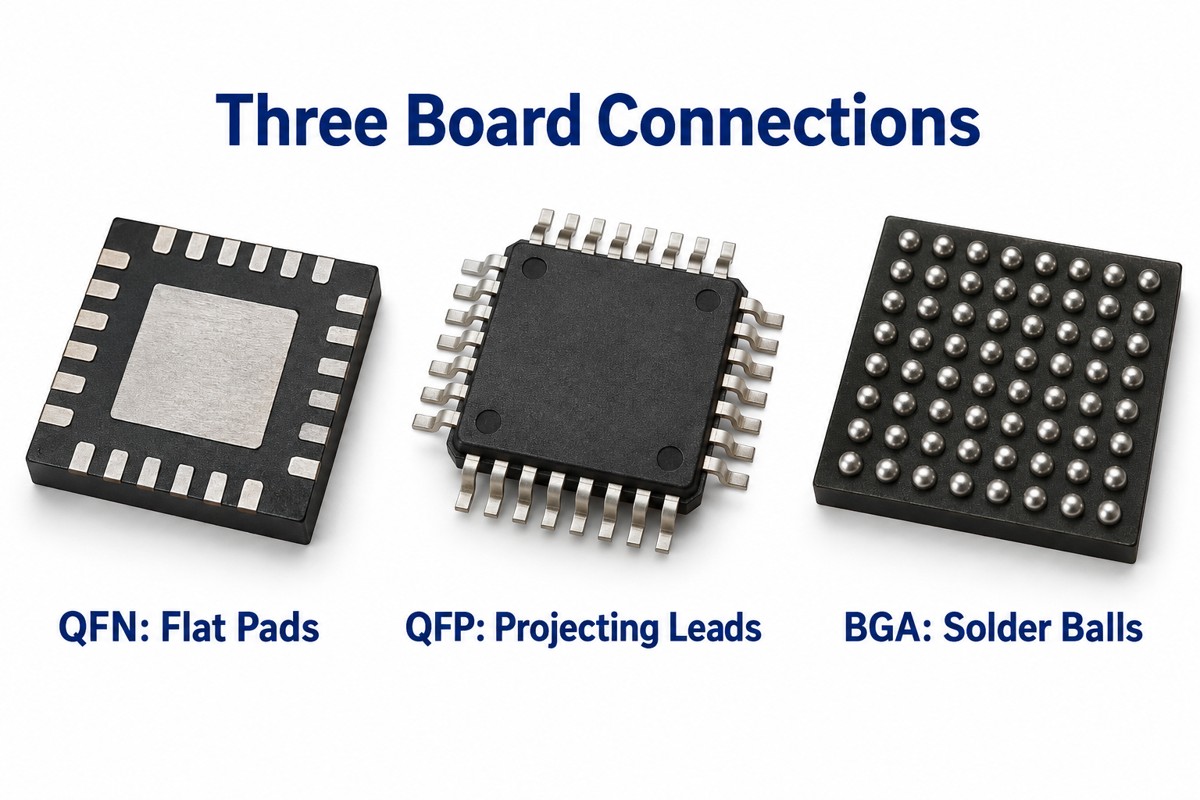
Package Board connection Contact arrangement
QFN Flat solderable terminals Four underside edges
DFN / SON Flat solderable terminals Two opposite underside edges
QFP Projecting gull-wing leads Four sides outside the body
BGA Solder balls Array beneath the body
QFN flat pads compared with QFP projecting leads and BGA solder balls

How Do Signals Travel Through a QFN Package?

In a conventional wire-bonded QFN, signals travel from the silicon die through bond wires, leadframe terminals and solder joints to PCB copper.

The die sits on a metal paddle inside the molded body. Fine wires connect its bond pads to separate terminal fingers around that paddle. After assembly, solder joins each bottom terminal to its corresponding PCB land. The signal path and the main downward heat path therefore use different parts of the package.

A flip-chip QFN replaces the internal bond-wire connection with bumps or copper pillars. That does not make its external board connection a BGA. The component can still have flat underside terminals. Check the manufacturer’s construction description when internal inductance, current paths or thermal behavior affect the circuit.

QFN Package Process Flow

A typical wire-bonded QFN package process flow includes die attachment, wire bonding, molding, package separation and testing. This semiconductor packaging process takes place before PCB assembly.

  1. Attach the die: secure the silicon to the leadframe’s die pad.
  2. Make internal connections: bond wires from die pads to terminal fingers.
  3. Mold the body: protect the die and wires while retaining the designed external contact surfaces.
  4. Separate the packages: use the specified saw or punch process.
  5. Inspect and test: check finished components before packing for board assembly.

Plating, marking and test order vary by package process. At EBest Circuit, our relevant service is mounting the finished IC onto your PCB, not fabricating the semiconductor die or its molded QFN package. This distinction matters when preparing an RFQ: we need the complete component part number and board assembly files.

QFN Package Dimensions: A 3 × 3 mm Example

The TI TPS62130 uses a nominal 3 × 3 mm, 16-terminal VQFN with 0.5 mm pitch. Its RGT package drawing shows why the terminal count alone cannot define a footprint.

Drawing item RGT0016C example
Body length and width 2.9–3.1 mm each
Terminal count 16 perimeter terminals
Terminal pitch 0.5 mm
Maximum package height 1.0 mm
Exposed-pad dimension 1.68 ± 0.07 mm square

These are package dimensions from the cited drawing, not universal QFN dimensions or ready-made PCB pad sizes. For a production release, match the complete orderable part number to its current drawing revision. A QFN package datasheet may provide separate package-outline, land-pattern and paste-layout pages; each serves a different purpose.
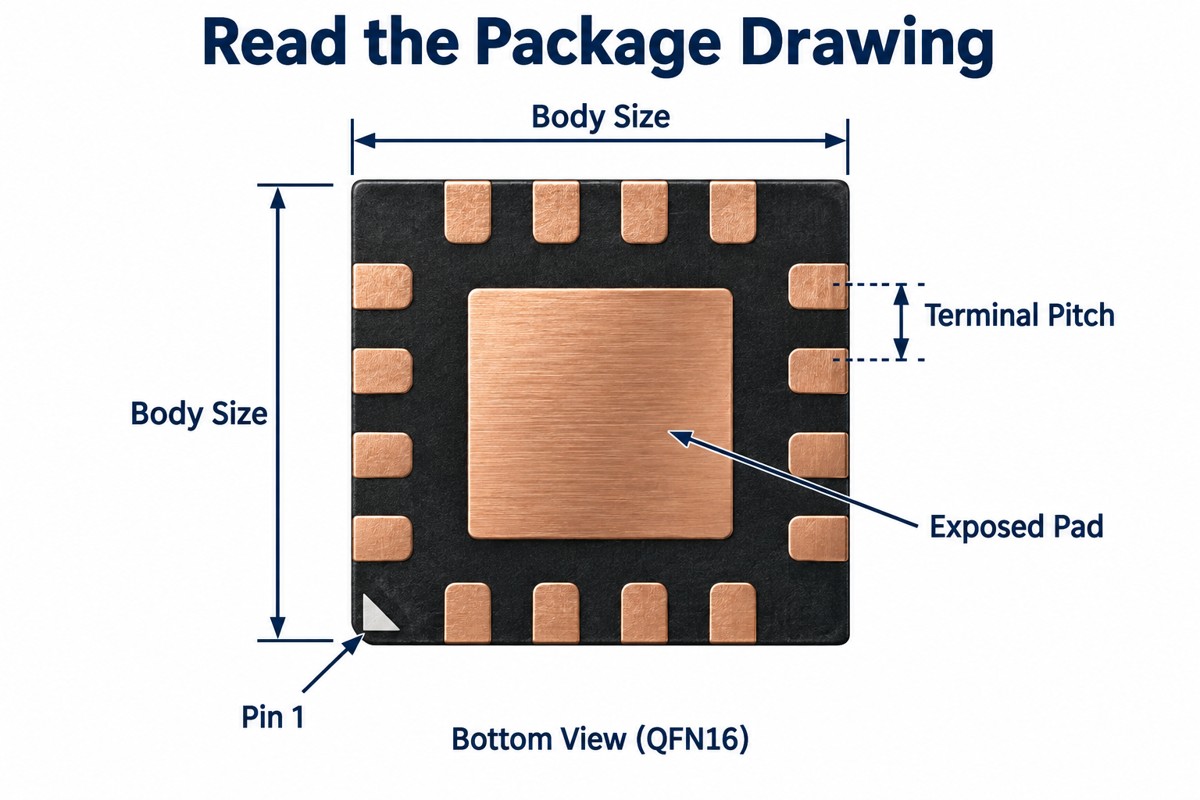
Simplified QFN bottom view identifying body size, terminal pitch, exposed pad and pin 1

What Does the Exposed Pad Do?

The exposed pad provides a short heat path from the die into the board and may also carry a required electrical connection.

For the TPS62130 example, the thermal pad connects to ground as directed by its datasheet. Do not transfer that connection to another IC by assumption. A different device may assign its exposed pad a different potential or give specific isolation instructions.

The complete heat path includes the die attachment, package paddle, solder joint, PCB copper and surrounding environment. Thermal vias can connect the top land to internal or opposite-side copper, but their treatment affects soldering. An open hole within the paste area can drain solder during reflow. Via location, plugging or filling must therefore be agreed with the PCB fabricator and assembler rather than added as an isolated layout detail.

How Does the Package Drawing Become a PCB Footprint?

The package drawing defines the component; the recommended land pattern translates that geometry into PCB copper and solder-mask openings.

Start with the exact manufacturer’s land pattern, then review fabrication tolerances and assembly access. Copying the body outline into a footprint does not establish a solderable connection.

  • Terminal lands: match the pin numbering and pitch, then check pad length and width against the recommended pattern.
  • Center land: use the specified electrical net and review its separation from perimeter pads.
  • Solder mask: check clearance and whether the intended mask webs can be manufactured.
  • Thermal vias: define hole position and treatment in the fabrication notes.
  • Placement data: verify pin 1, centroid rotation and the assembly drawing together.

Our broader QFN package guide covers additional package families and size-selection questions. For the board release itself, keep the component drawing, copper land and paste aperture data as separate checks.

How Should Solder Paste Be Divided Under a QFN?

Use separate peripheral apertures and segmented openings over the exposed pad, with the total paste volume matched to the component’s assembly guidance.

TI’s QFN and SON PCB Attachment guide gives approximately 50–70% exposed-pad paste coverage as a typical design approach. This is a starting point from that guide, not a universal acceptance limit. A full-size central opening can deposit too much paste and lift the body, leaving insufficient contact at the outer terminals.
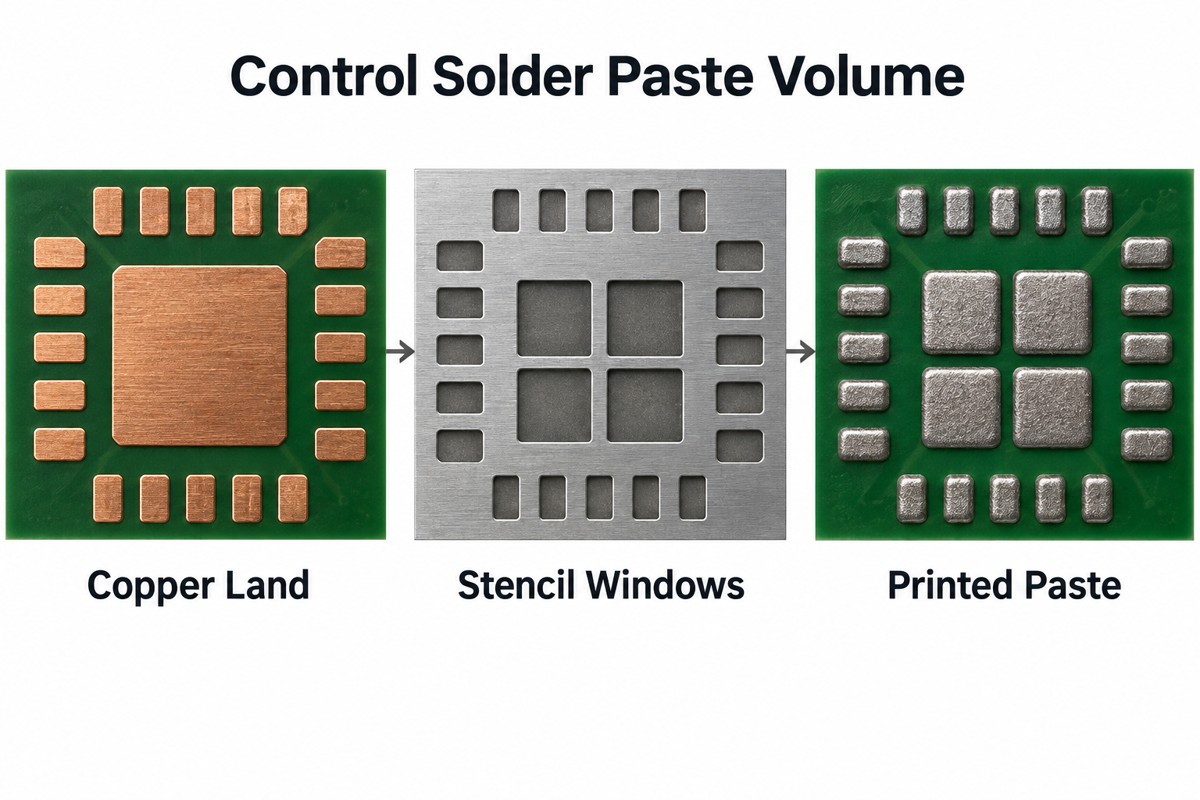
Copper land, divided stencil windows and printed paste shown as separate QFN assembly layers

Coverage describes the printed opening area relative to the center land. Voiding describes gaps in the solder joint after reflow. They are not interchangeable percentages. Stencil thickness also changes deposited volume, so identical coverage can produce different results with different foils.

Our SMT stencil service supports the printing stage of PCB assembly. For QFN package soldering, review the paste layer alongside the board design, then check actual deposits with SPI before placement. The reflow profile must suit the solder paste while respecting the component’s temperature and moisture-handling limits.

What Changes When a QFN Has Wettable Flanks?

Wettable flanks provide solderable side features that make perimeter fillets easier to inspect optically.

A conventional sawn terminal may expose bare copper at its side. That surface does not always form a visible fillet, even when the bottom connection is soldered. Pull-back terminals sit inward from the body edge and do not offer the same side-view access.

Wettable-flank versions use features such as plated steps or dimples to support visible solder formation. Confirm the feature in the exact package specification and use its matching land pattern. Side fillets help AOI evaluate the perimeter, but they do not show the entire soldered center pad beneath the body.

How Are Hidden QFN Joints Checked?

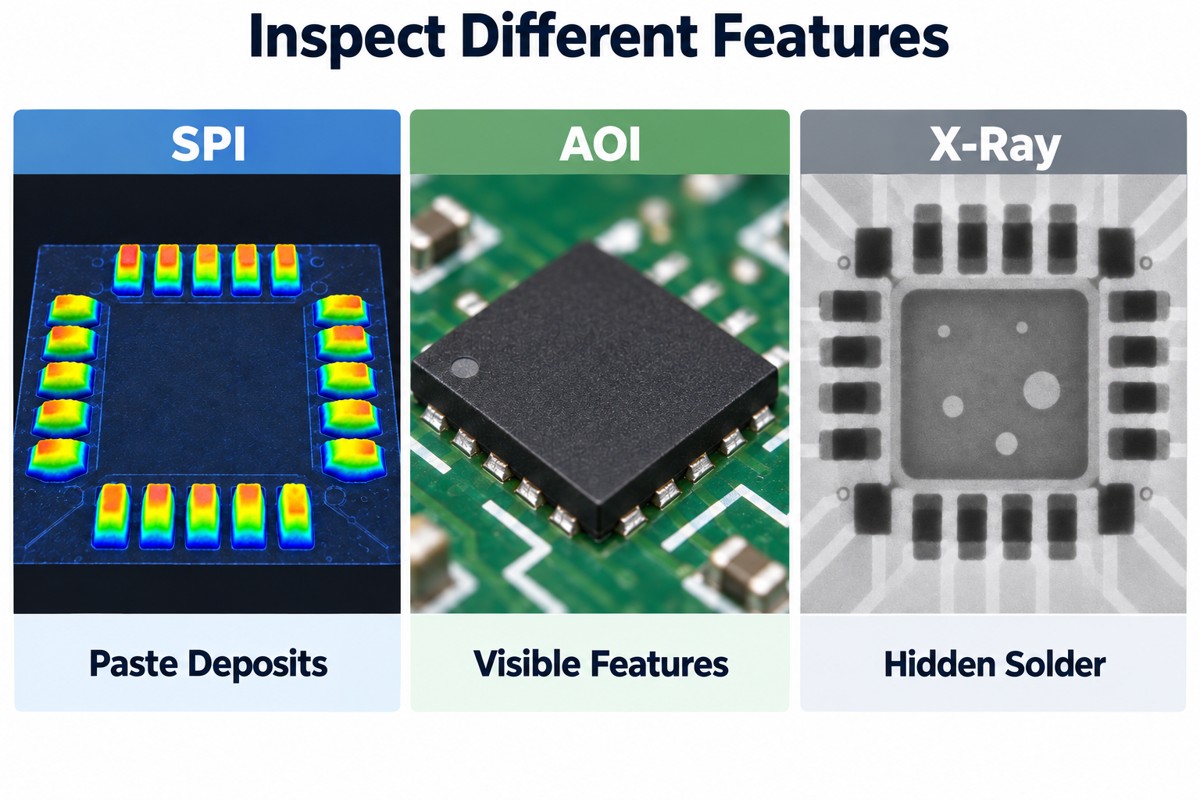
X-ray inspection examines hidden QFN solder features, while electrical or functional testing checks circuit behavior. Neither replaces control of the paste-printing process.

Method Primary check
SPI before placement Paste volume, height, area and position
AOI after reflow Orientation, placement and accessible solder features
X-ray after reflow Hidden solder distribution, bridges and void patterns
Electrical / functional test Specified connections and operating behavior
Illustrative SPI paste deposits, AOI visible features and X-ray hidden solder inspection

A void limit must come from the applicable component guidance and agreed product requirements. Total void area alone cannot describe every thermal or reliability concern. Location, distribution and the heat-flow path also matter. A normal-looking 2D projection cannot prove every interface has wetted correctly.

At EBest Circuit, we have 3D SPI, AOI and X-ray inspection resources for PCBA work. We establish the inspection and test scope for the actual assembly rather than treating one passing image as evidence that every requirement has been met.

FAQ About Quad Flat No Leads Packages

Does QFN mean the package contains no lead metal?
No. “No-lead” refers to external connection geometry. Lead-free status concerns materials and must be checked in the manufacturer’s environmental declaration or orderable-part information.

Can I solder a QFN using only a soldering iron?
An iron may reach some perimeter contacts, but it usually cannot form the hidden center-pad joint properly. A controlled reflow or rework process is more suitable when the underside pad must be soldered.

Can a QFN be replaced after assembly?
Yes, with a qualified rework process. Heat all solder joints sufficiently before lifting the package, clean and inspect the lands, then control paste deposition and alignment for replacement. Pulling before the joints melt can damage PCB pads.

Does a 260°C package rating mean I should set every reflow zone to 260°C?
No. A package-body temperature limit is not an oven-zone recipe. Use the paste supplier’s profile guidance and measure the assembled board’s actual temperature history without exceeding component limits.

Can conformal coating correct a weak QFN solder joint?
No. Coating protects against specified environmental exposure; it cannot replace a missing electrical connection or restore the intended thermal solder path. Inspect and resolve assembly defects before coating.

How Can EBest Circuit Support Your QFN PCB Assembly?

We can support the board-level work around your selected QFN: PCB fabrication, component sourcing, stencil preparation, SMT assembly and the agreed inspection and testing.

Send your Gerber or ODB++ files, BOM with full manufacturer part numbers, pick-and-place data and quantities to sales@bestpcbs.com. Include any exposed-pad, thermal-via or inspection requirements. We can review those details with you and prepare a quotation for the actual build.
You may also like

QFN Package Guide: Meaning, Sizes, PCB Design & Soldering
Wednesday, July 29th, 2026

QFN packages are common in power-management ICs, sensors, RF devices, motor drivers, and compact controllers. Their small footprint and short electrical paths make them useful when board space is limited. The trade-off is assembly sensitivity: most joints sit beneath the package, so footprint design, paste control, reflow, and inspection matter more than they do with leaded packages.

This guide explains what QFN means, how the package is built, how to read its datasheet, and how to design and assemble a reliable QFN PCB. It also compares QFN with QFP and BGA so engineers and buyers can choose a practical package rather than simply selecting the smallest option.

QFN package guide covering meaning, PCB design and soldering

What Is a QFN Package?

QFN stands for Quad Flat No-Lead. It is a surface-mount IC package with terminals placed around the bottom perimeter instead of extending from the sides.

Many QFN packages also include a large exposed pad in the center. This pad may:

  • Transfer heat from the die into the PCB
  • Provide a ground or power connection
  • Improve mechanical support after soldering

QFN describes the package, not the function of the chip. Voltage regulators, sensors, amplifiers, wireless ICs, microcontrollers, and interface devices may all use the same package family.

The package saves board space and keeps signal paths short. Its hidden joints, however, demand accurate lands, balanced paste, and planned inspection.

How Is a QFN Package Constructed?

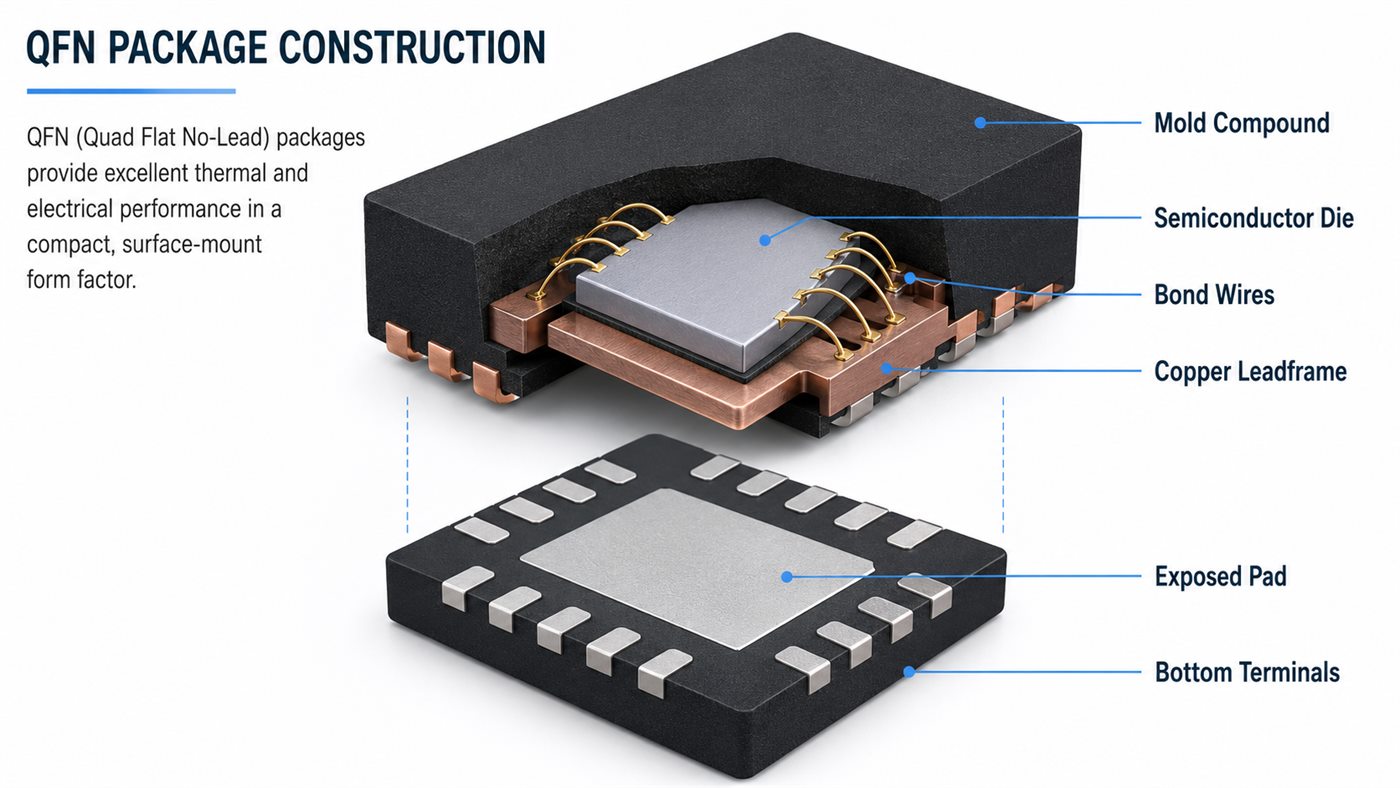
A standard wire-bonded QFN is built around a copper leadframe. The semiconductor die sits on a central paddle, while fine wires connect the die to the surrounding terminals. Mold compound protects the internal structure.

The main elements are:

  • Semiconductor die
  • Copper leadframe
  • Die-attach material
  • Bond wires or flip-chip interconnects
  • Mold compound
  • Bottom perimeter terminals
  • Exposed center pad

Sawing or punching separates the package from the leadframe strip and affects whether the terminal sidewall forms a visible solder fillet. Because QFNs offer little mechanical compliance, pad geometry, board flatness, solder volume, and reflow behavior directly affect joint quality.

QFN package construction showing mold compound, semiconductor die, bond wires, copper leadframe, exposed pad and bottom terminals

What Are the Main QFN Package Types?

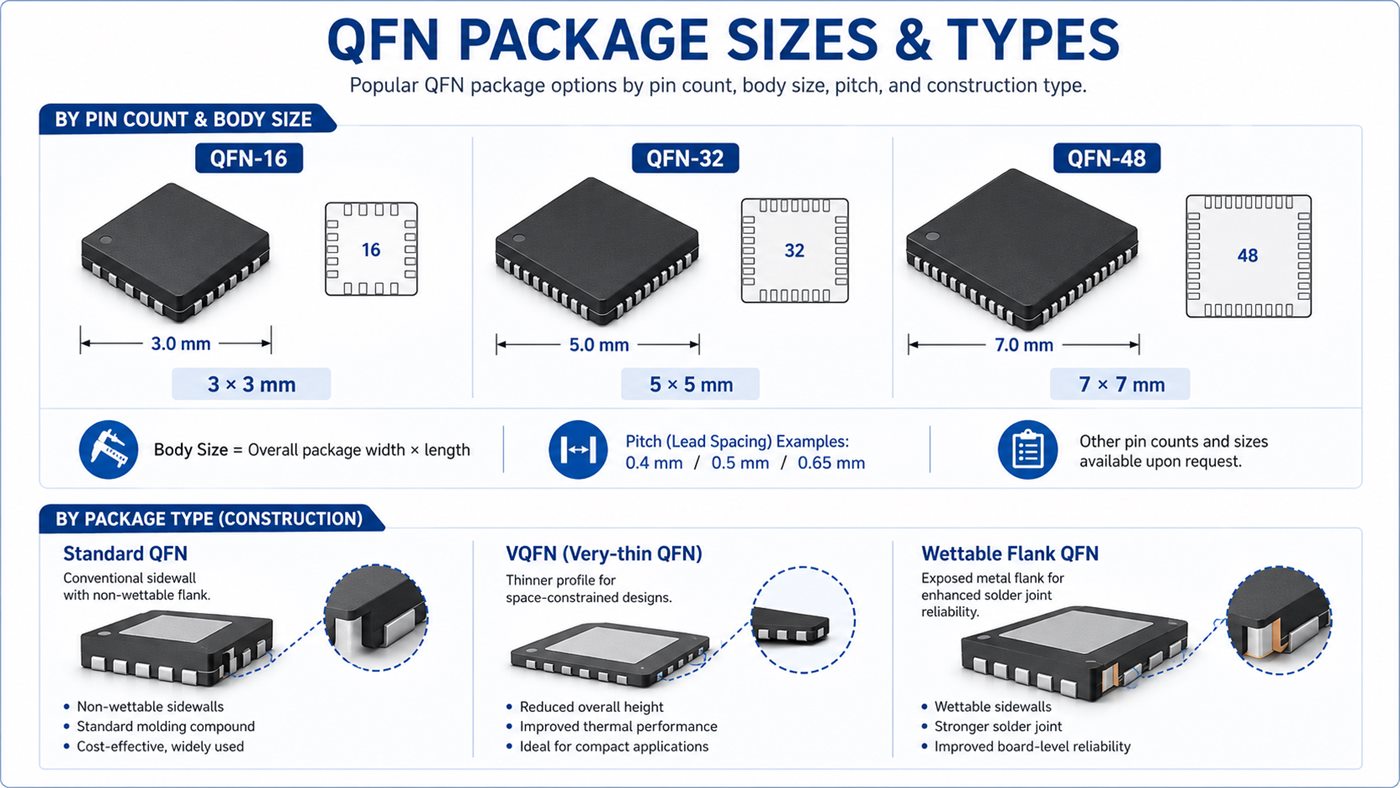
Each QFN package type may use different body dimensions, terminal geometry, and assembly controls. QFN names vary between semiconductor manufacturers. A supplier may use VQFN, TQFN, WQFN, or XQFN for a specific thickness or footprint family, but those labels are not universal standards.

QFN type Main feature Design note
Standard QFN Bottom perimeter pads and center pad Common for general SMT designs
VQFN Very thin body Useful where height is restricted
TQFN Thin package profile Check the supplier’s exact height
XQFN Very small body and pitch Needs tighter printing and placement control
FCQFN Flip-chip internal connection Can reduce internal path length
Multi-row QFN More than one terminal row Higher I/O density and harder routing
Power QFN Large current or thermal terminals Requires careful copper and heat-flow design
Wettable flank QFN Solderable terminal sidewall Improves optical inspection

VQFN vs QFN

VQFN usually means Very Thin Quad Flat No-Lead. It is still part of the QFN family.

The “V” mainly refers to package height. It does not guarantee better thermal performance, easier soldering, or footprint compatibility. Use the exact package drawing for the selected part number.

What QFN Package Sizes, Pin Counts, and Pitches Are Available?

QFN package dimensions vary by manufacturer and part number. QFN packages come in square and rectangular forms with many body sizes, pin counts, heights, and pitches. Common terminal pitches include 0.4, 0.5, 0.65, and 0.8 mm.

A description such as QFN-32, 5 × 5 mm, 0.5 mm pitch normally means:

  • 32 terminals
  • 5 mm body length
  • 5 mm body width
  • 0.5 mm terminal spacing

It does not define the terminal length, terminal width, exposed-pad dimensions, or package height.

Two 5 × 5 mm packages may still need different footprints. Fine-pitch versions can require narrower mask dams, finer paste, better stencil release, higher placement accuracy, and more careful inspection. Select the package with the assembler’s real process capability in mind.

QFN package sizes, pin counts, pitches and package types including VQFN and wettable flank QFN

How Do You Read a QFN Package Datasheet?

Start with the mechanical package drawing, not a generic footprint library. Check the following items before layout:

  • Full package code
  • Complete manufacturer part number
  • Terminal count and numbering
  • Body length and width
  • Package height
  • Terminal pitch
  • Terminal width and length
  • Exposed-pad size
  • Pin 1 marking
  • Dimensional tolerances
  • Recommended land pattern
  • Paste-mask guidance
  • Moisture sensitivity level
  • Maximum reflow temperature

Do not copy a footprint from another QFN because the body size matches; terminal length, paddle size, corner geometry, and tolerances may differ.

For purchasing and quotation, provide the full manufacturer part number. “QFN-32” alone is insufficient.

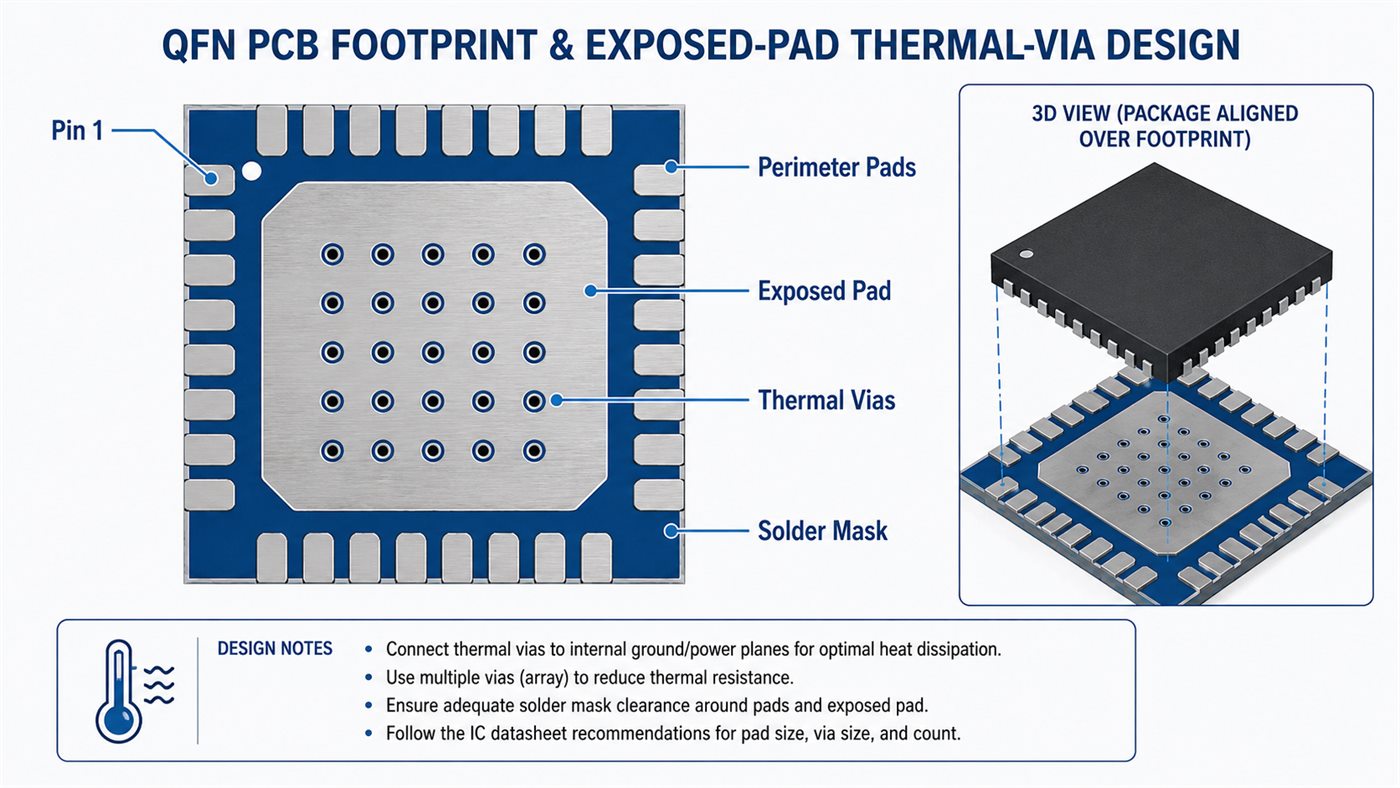
How Should a QFN PCB Footprint Be Designed?

Use the component manufacturer’s recommended land pattern as the starting point. Then check whether it is practical for the chosen PCB and SMT process.

Review these points:

  • Match pad count, pitch, width, and position to the package drawing.
  • Add a clear pin 1 mark that remains visible after placement.
  • Confirm whether solder-mask-defined or non-solder-mask-defined pads are required.
  • Check whether the PCB supplier can hold the solder mask dams.
  • Avoid excessive toe extension, which can encourage solder balls or movement.
  • Leave enough courtyard space for placement, inspection, and rework.
  • Route high-current pins with suitable copper width.
  • Review the paste layer separately from the copper layer.

The center land may need segmentation for thermal vias and paste control. DFM review should examine the footprint, mask, stencil, via treatment, package tolerance, and inspection method together.

How Should the Exposed Pad and Thermal Vias Be Designed?

The exposed pad often carries heat from the IC into the PCB. Many devices are rated on the assumption that this pad is properly soldered.

First confirm its electrical function. It may connect to:

  • Ground
  • Power
  • A switching node
  • A thermal-only copper area

Never connect it to ground by assumption.

Thermal-via design should consider:

  • Device power dissipation
  • Exposed-pad area
  • PCB thickness
  • Copper thickness
  • Internal ground or power planes
  • Junction-temperature limit
  • Enclosure temperature
  • Airflow
  • Via fill or plug method

Open vias inside the paste area can pull solder away from the joint. This may cause low solder coverage, uneven standoff, or solder leakage to the opposite side.

For via-in-pad designs, state whether vias are filled, capped, plugged, or left open in both fabrication notes and quotation data. Extra vias can add cost after the design already has an effective thermal path.

QFN PCB footprint with perimeter pads, exposed thermal pad, thermal vias, solder mask and pin 1 marker

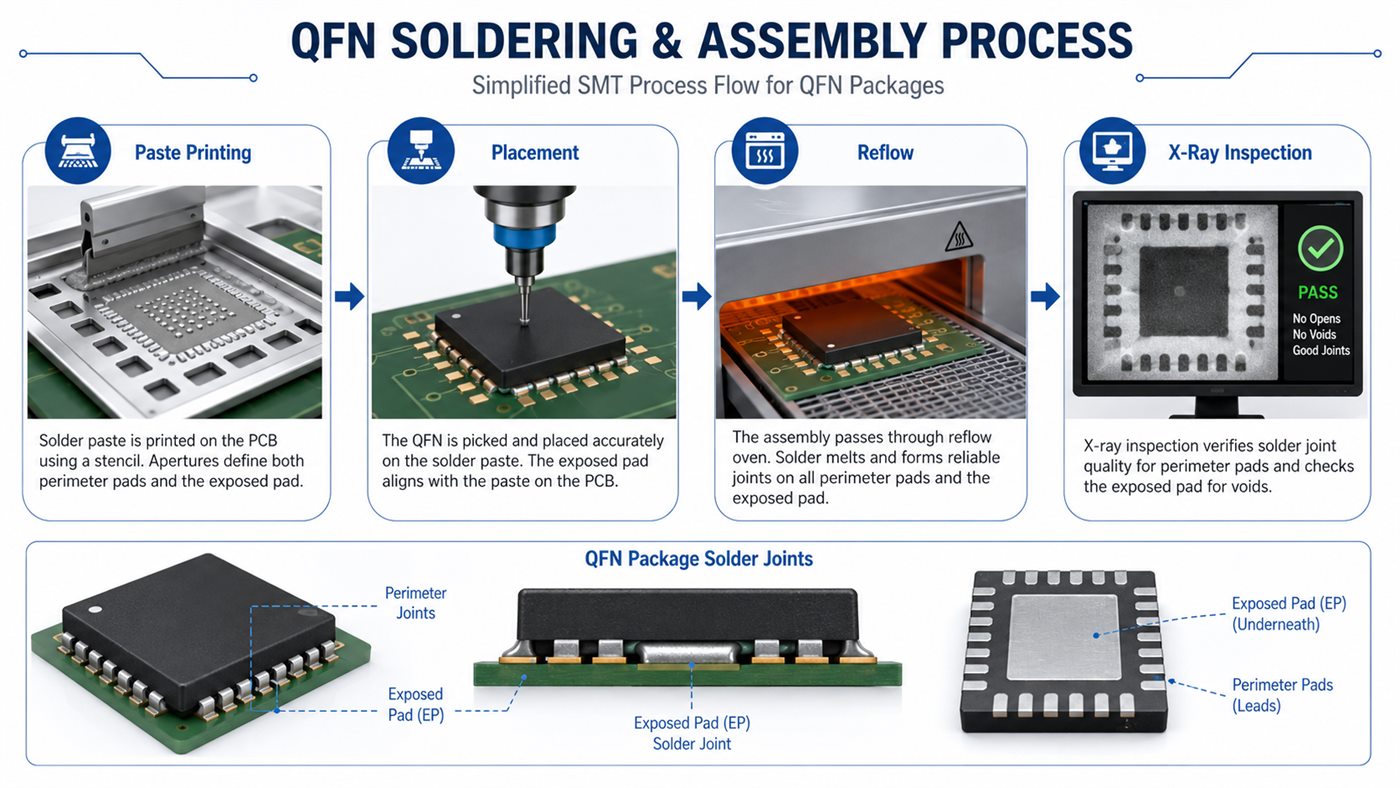
How Is a QFN Package Soldered?

Production QFN package soldering normally follows a controlled SMT process:

  • Check moisture sensitivity and baking requirements.
  • Print solder paste through a designed stencil.
  • Use SPI to inspect paste volume and position.
  • Place the component with automated equipment.
  • Reflow with a profile matched to the paste and component limits.
  • Use AOI for orientation and visible features.
  • Use X-ray for hidden joints and the center pad.
  • Perform electrical or functional testing when required.

Placement pressure must be controlled. Too much force can squeeze paste away from the terminals. Too little can leave the package unstable before reflow.

Manual soldering is possible for prototypes using hot air, a hot plate, or a small reflow oven. It is less suitable when the project requires repeatable void control, thermal verification, inspection records, or production traceability.

A working prototype may still have poor center-pad coverage, so function alone does not prove production readiness.

QFN soldering and SMT assembly process from paste printing and placement to reflow and X-ray inspection

How Should a QFN Stencil and Solder Paste Pattern Be Designed?

The stencil must balance solder volume between the perimeter pads and the exposed center pad. Too much center-pad solder can lift the package and create open joints around the edge.

A window-pane pattern is commonly used under the exposed pad. Several smaller apertures help distribute paste more evenly and reduce component float.

Key variables include:

  • Stencil thickness
  • Aperture dimensions
  • Aperture area ratio
  • Total center-pad paste coverage
  • Spacing between center apertures
  • Perimeter-pad paste reduction
  • Solder paste powder size
  • Stencil wall finish
  • Print speed and separation settings

For fine-pitch QFNs, base the final pattern on the component application note and the assembler’s validated process, not a universal paste percentage.

What Are the Most Common QFN Soldering Defects?

QFN defects usually come from several process variables acting together.

Defect Common cause Inspection Typical correction
Center-pad voiding Trapped volatiles or poor aperture design X-ray Revise stencil or reflow profile
Open perimeter joint Low paste, package float, poor wetting X-ray or electrical test Rebalance paste and placement
Solder bridge Excess paste or poor spacing AOI or X-ray Reduce aperture or review footprint
Component shift Uneven paste or placement offset AOI Balance apertures and alignment
Excessive standoff Too much center-pad solder X-ray or cross-section Reduce center-pad paste
Solder wicking Open vias under the pad X-ray or cross-section Fill, cap, plug, or move vias
Low center-pad coverage Poor print or via drainage X-ray Improve printing and via treatment
Non-wetting Oxidation, contamination, or poor profile Visual, X-ray, or cross-section Review storage, finish, flux, and reflow

Void percentage alone does not tell the full story. Void location and its effect on the heat path may matter more than total area.

How Are QFN Solder Joints Inspected?

No single method finds every QFN defect.

  • AOI: Checks orientation, placement, contamination, and visible side fillets.
  • X-ray: Reveals center-pad voiding, bridges, missing solder, and gross alignment problems.
  • Electrical test: Confirms continuity and device response.
  • Functional test: Confirms that the assembled board performs under defined conditions.
  • Cross-section: Shows wetting, joint height, void location, and plating condition.
  • Dye-and-pry or destructive analysis: Used for qualification or failure analysis.

Inspection requirements should be agreed before quotation. X-ray reporting, void criteria, sample size, and record retention can affect price and lead time.

What Is a Wettable Flank QFN?

A wettable flank QFN has processed terminal sidewalls that allow solder to form a visible side fillet after reflow.

This helps AOI confirm the perimeter joints. It is especially useful in automotive and other high-reliability assemblies where optical inspection coverage is important.

Wettable flanks improve joint visibility, but they do not replace correct footprints, paste control, stable reflow, X-ray, or electrical testing. Confirm the feature in the datasheet or package code.

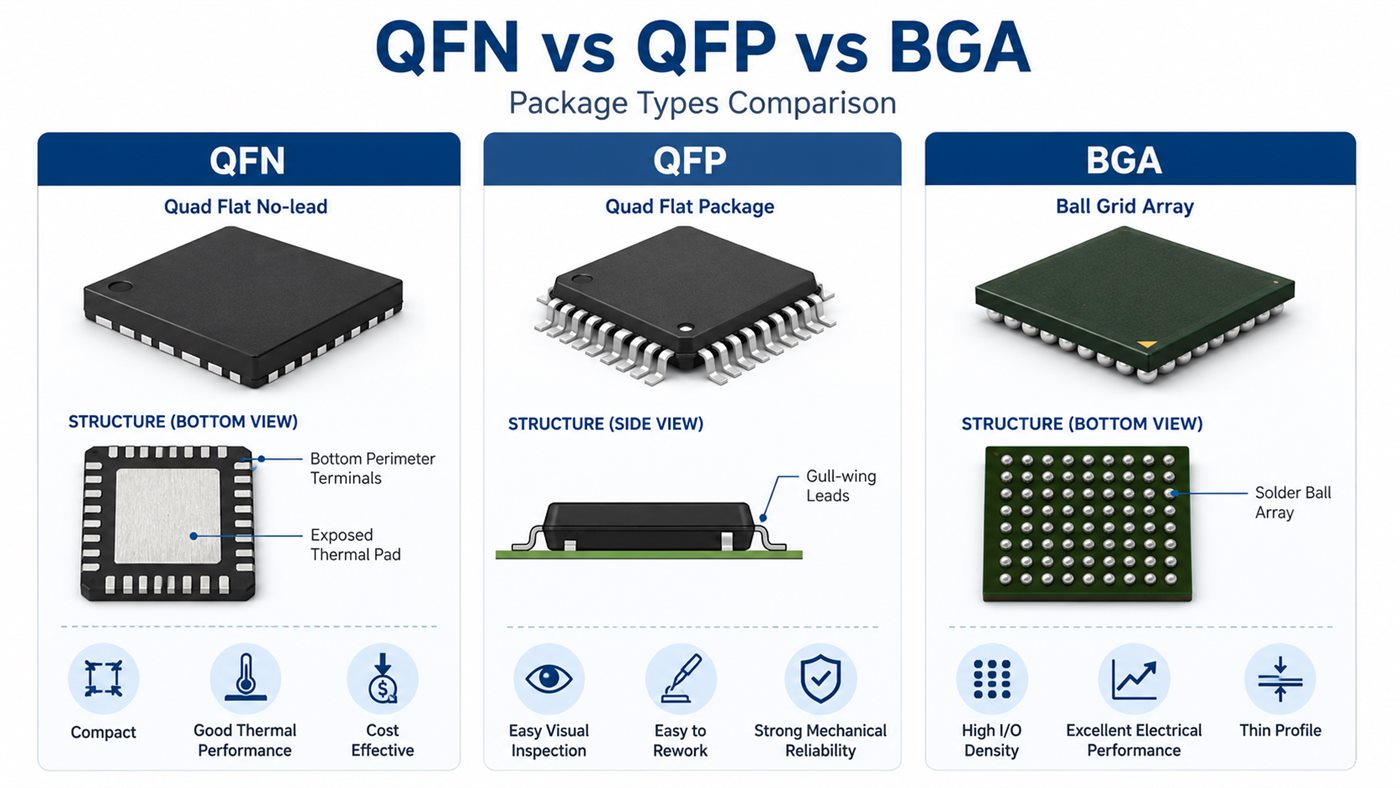
QFN vs QFP: What Is the Difference?

The main choice is between QFN compactness and QFP accessibility.

Comparison QFN QFP
Terminal structure Bottom perimeter lands External gull-wing leads
Board area Usually smaller Usually larger
Package height Often lower Often higher
Electrical path Shorter Longer external leads
Visual inspection Limited Easier
Hand soldering More difficult Easier
Lead damage No protruding leads Leads can bend
Thermal path Often uses an exposed pad Package-dependent
Rework More process-sensitive More accessible
Best fit Compact production designs Development and repair-friendly designs

Choose QFN when board space, package height, electrical path length, or exposed-pad heat transfer matters most. Choose QFP when visible joints, hand assembly, probe access, and easier repair are more important.

QFN vs BGA: Which Package Should You Choose?

The main decision is I/O density versus routing and assembly complexity.

Comparison QFN BGA
Connection layout Perimeter terminals Area-array solder balls
Typical I/O density Low to medium Medium to very high
Escape routing Relatively direct May require more layers or via-in-pad
PCB cost Often lower Can rise with routing complexity
Inspection AOI plus X-ray Mainly X-ray for hidden joints
Rework Difficult More specialized
Prototype suitability Practical with capable SMT equipment Strongly depends on pitch and PCB design
Typical use Power, analog, RF, sensors, controllers Processors, FPGAs, memory, high-I/O ICs

Use QFN when the device pin count fits a perimeter layout and the project benefits from a compact package. Use BGA packaging when the design needs substantially more I/O in a limited area.

QFN vs QFP vs BGA package comparison showing terminal structures and typical strengths

How Do You Choose the Right QFN Package for a PCB Project?

Package selection should fit the device, PCB process, inspection plan, and future volume.

Before design release, confirm:

  • Complete manufacturer part number
  • Package code and lifecycle status
  • Body size, height, pitch, and pin count
  • Power dissipation and junction-temperature limit
  • Exposed-pad electrical function
  • Thermal-via and plane requirements
  • PCB layer count and routing space
  • Solder mask and stencil capability
  • AOI and X-ray requirements
  • Prototype and production quantities
  • Rework expectations
  • Reliability or automotive requirements
  • Wettable-flank availability
  • Moisture sensitivity and storage needs

For a useful PCBA quotation, provide:

  • Gerber or ODB++ files
  • BOM with complete manufacturer part numbers
  • Pick-and-place file
  • Assembly drawing
  • Target quantity
  • Test requirements
  • X-ray or void-reporting criteria
  • Any via-fill or special stencil requirements

At EBest Circuit, reviewing the footprint, thermal vias, stencil, component availability, and inspection plan before layout release helps avoid redesign after prototype assembly.

FAQs About QFN Packages

What does QFN stand for?

QFN stands for Quad Flat No-Lead. It is a surface-mount IC package with terminals positioned mainly around the underside perimeter. Many versions also include an exposed center pad for thermal or electrical connection.

Is QFN the same as QFP?

No. QFN terminals are located beneath the package, while QFP packages use external gull-wing leads on all four sides. QFN saves board space, but QFP joints are easier to inspect and rework.

Is VQFN better than a standard QFN?

Not automatically. VQFN usually identifies a very thin package, which is useful for height-restricted products. It does not necessarily improve solderability, thermal performance, or reliability. The exact supplier package drawing must be checked.

Does the exposed QFN pad have to be soldered?

In most thermally enhanced QFN designs, yes. The manufacturer’s thermal data may assume that the pad is soldered to the PCB. Its electrical connection must be taken from the component datasheet rather than assumed.

Can QFN packages be soldered by hand?

Yes, especially for prototypes, using hot air, a hot plate, or a controlled reflow method. Hand soldering is less suitable when repeatable center-pad coverage, low voiding, inspection records, or production reliability is required.

How do you inspect solder joints under a QFN?

Use a combination of AOI, X-ray, electrical testing, and functional testing. X-ray is especially useful for examining the exposed center pad and hidden perimeter joints. Cross-section analysis may be used for qualification or failure investigation.

What causes voids under a QFN thermal pad?

Typical causes include flux volatiles, a single oversized stencil opening, excessive paste, unsuitable reflow conditions, and solder loss into open vias. The location and thermal effect of the voids matter as much as their total area.

Is QFN better than BGA?

QFN is often simpler and less expensive for devices with moderate pin counts. BGA is better suited to high-I/O components that require an area-array connection. The right choice depends on device availability, routing density, PCB layers, inspection, and rework capability.

Conclusion

QFN packages provide a compact footprint, short electrical paths, and an effective thermal connection to the PCB. Reliable results depend on matching the exact package drawing with the footprint, thermal-via structure, stencil, reflow process, and inspection plan.

For QFN PCB design review, prototype assembly, or a production quotation, send your Gerber files, BOM, placement data, and test requirements to EBest Circuit at sales@bestpcbs.com.

You may also like