PCB manufacturing PCB manufacturing
Home > Blog

PCB BOM

PCB BOM Management for Reliable PCBA Production
Tuesday, September 1st, 2026

PCB BOM management becomes most important when a prototype turns into recurring PCBA production. At that stage, buyers are not only asking who can assemble boards. They need a supplier who can keep component information controlled, watch sourcing risks, handle approved alternatives, and prevent design engineers from being pulled back into every reorder.

For many buyers, the real pain starts between orders. A part goes out of stock, an IC becomes long-lead, a connector needs a replacement, or an old BOM revision returns during repeat production. If the supplier only reacts after a purchase order is placed, the project can lose time quickly. This guide explains how BOM control affects quotation, sourcing, assembly, lead time, repeat orders, and how EBest Circuit supports BOM-to-PCBA production with practical manufacturing follow-up.
PCB BOM management
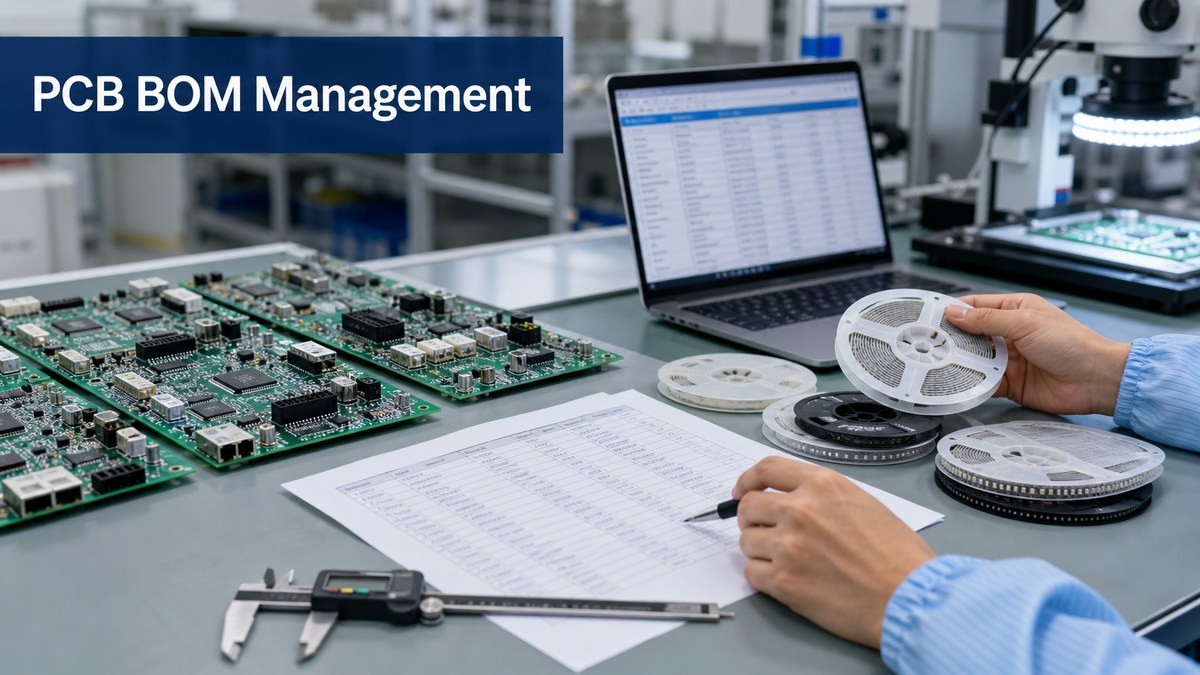
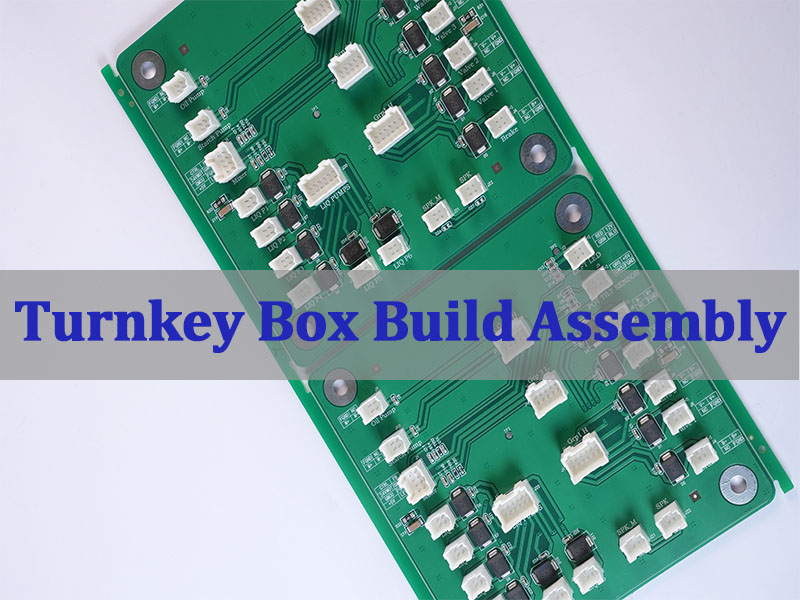
PCB BOM management helps connect component data, sourcing risk, and PCBA production before the order reaches the line.

Why PCB BOM Management Matters Before Production

The BOM is the bridge between engineering files and real PCBA production. Gerber files define the PCB, but the BOM tells the supplier what must be purchased, mounted, inspected, tested, and repeated in the next batch.

For a buyer, strong BOM control helps answer practical questions before money and time are committed:

  • Can each part be identified by a complete manufacturer part number?
  • Are approved brands, values, packages, and tolerances clear?
  • Are any parts obsolete, NRND, long-lead, or hard to source?
  • Are alternative parts allowed, and who can approve them?
  • Does the BOM match the CPL, assembly drawing, and PCB footprint?
  • Will the quoted lead time still work after real sourcing checks?

A BOM problem is not only a spreadsheet problem. It can force the production material list to change, require MRP to run again, delay material kitting, increase warehouse communication, and create avoidable inventory cost. That is why BOM review should happen before PCBA production, not after the SMT line is ready.

PCB BOM Details Buyers Should Confirm

A good PCB BOM should be clear enough for quotation, purchasing, assembly, inspection, and repeat production. If a supplier has to guess, the quotation may look fast, but the risk is only pushed later.

Buyers should confirm these details before sending an RFQ:

BOM Detail Why It Matters
Manufacturer part number Reduces wrong-part purchasing
Quantity per board Affects total component cost
Package and footprint Helps match pads and SMT process
Value and tolerance Avoids electrical mismatch
Polarity or orientation Reduces assembly mistakes
Approved alternatives Speeds shortage response
DNI/DNP parts Prevents unwanted mounting
Revision number Keeps all files aligned

The most useful BOM is not the longest BOM. It is the BOM that removes guessing. For PCBA buyers, complete part numbers, controlled alternatives, clear mounting status, and revision discipline usually matter more than extra notes that no one can act on.

BOM in PCB Assembly Issues That Stop Production

Many PCBA delays start with small BOM issues that were not visible during the first quotation. Once parts are being purchased and the job is moving toward production, these issues can stop the build.

Common problems include:

  • a distributor code is listed instead of the real manufacturer part number
  • the part value is clear, but package size is missing
  • the BOM says one connector, while the footprint matches another
  • the CPL direction does not match the silkscreen or datasheet
  • a polarized component has no clear orientation note
  • the customer changed the BOM but did not update the assembly drawing
  • a substitute part is available, but it has not been approved
  • a test point, programming connector, or fixture requirement is missing

These problems affect more than purchasing. They can delay SMT programming, stencil confirmation, first article inspection, functional testing, and final shipment. A supplier that catches these problems before production helps the buyer avoid expensive “stop and clarify” moments.

For controlled PCBA production, BOM information also needs to reach the workshop correctly. Material verification, inspection records, and anti-wrong-material checks help reduce the risk that an approved BOM is interpreted one way by purchasing and another way on the production floor.

BOM Issues That Change Your PCBA Quote

A PCBA quote is only reliable when the BOM is reliable. If the BOM contains unclear, risky, or incomplete component information, the first price may not reflect the real build cost.

BOM issues can change the quote in several ways:

  • Wrong or missing MPN: the buyer may receive a price based on a different part.
  • Unclear package: SMT difficulty, stencil opening, or placement risk may change.
  • Shortage parts: spot-market sourcing may raise cost or reduce traceability.
  • MOQ or package type: reels, cut tape, tubes, trays, and loose parts affect purchasing and handling.
  • Unapproved substitutes: price may change after engineering approval.
  • Missing testing scope: fixture, programming, or functional test time may not be included.

This is why buyers should not evaluate a supplier only by the fastest initial quote. A responsible PCBA quote should expose BOM questions early, especially for connectors, ICs, power components, LEDs, relays, sensors, and parts with tight tolerance or lifecycle risk.

For repeat production, price breaks also depend on BOM stability. A quote for 50, 125, 250, or 500 units can change if a key part has limited stock, high MOQ, or a substitute that still needs approval. The earlier these risks are visible, the easier it is for the buyer to compare real production cost.
PCB BOM management
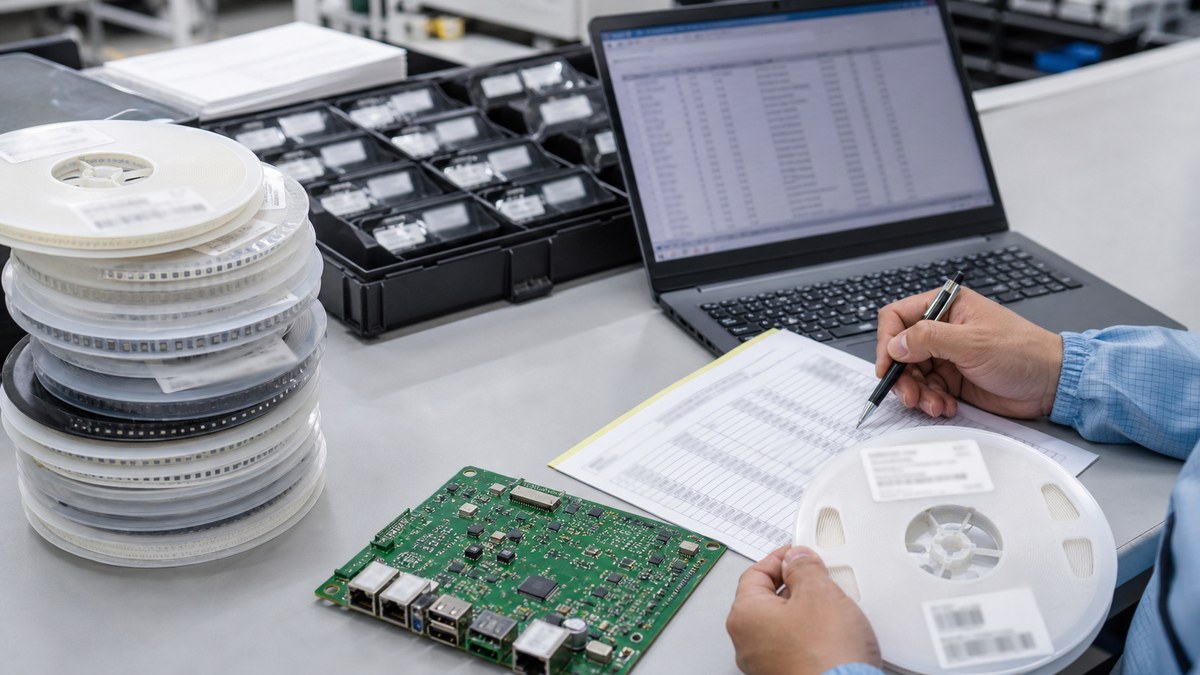
BOM review should be connected with component sourcing, approved alternatives, and material readiness.

Component Availability Before Purchasing

Component availability is one of the biggest differences between a “quoted BOM” and a “buildable BOM.” A BOM may look complete, but if key parts are out of stock, obsolete, restricted, or available only in small lots, the project can still stall.

For recurring PCBA production, availability should not be checked only after a purchase order arrives. Buyers often want the supplier to watch EOL, NRND, shortage, and long-lead risks between orders, especially when the same board is reordered again and again.

Before purchasing, EBest Circuit checks whether important components can be sourced with the required quantity, package, lead time, and supplier traceability. For high-risk parts, our team may return questions before buying instead of waiting until material shortage affects production.

Useful checks include:

  • stock status for key ICs and connectors
  • lead time for long-cycle components
  • MOQ and packaging method
  • lifecycle risk such as obsolete or NRND parts
  • supplier source and traceability needs
  • consistency between BOM, purchase request, PO, and production material list

For buyers, this step protects both cost and delivery. It also helps move sourcing responsibility away from the buyer’s design team and into a controlled manufacturing process.

Warehouse control matters here too. When receiving, storage, and material issuing are traceable, the BOM review is connected with real kitting status instead of staying as a spreadsheet discussion. This is especially useful when one missing reel, tray, tube, or through-hole part can hold the full PCBA batch.

Approved Alternatives for Shortage Parts

Alternative parts can save a project, but only when they are controlled. A random replacement can create electrical risk, assembly risk, testing failure, or customer approval problems.

A practical BOM should separate:

  • Preferred parts: the first choice for quotation and purchasing
  • Approved alternatives: parts already accepted by the customer
  • Temporary substitutes: used only for a specific batch or urgent order
  • Not-approved parts: available in the market but not allowed for production

Some buyers prepare a substitution authority before recurring production. This can define which parts may be replaced without delay, which parts need engineering approval, what data the supplier must provide, and whether the approval is valid for one batch or future repeat orders.

EBest Circuit can help buyers review alternative component options, but substitution should always stay under customer approval. For example, a resistor or capacitor may look easy to replace, but tolerance, voltage rating, temperature coefficient, package size, and brand restrictions can matter. For connectors, ICs, relays, sensors, and power devices, the approval threshold is usually higher.

Clear alternative rules help prevent a common production problem: purchasing uses one part, the production material list shows another, and engineering approval refers to a different BOM revision. When those three records do not match, the project becomes harder to control.

PCBA Lead Time Risks from BOM Problems

Lead time is often delayed before assembly starts. If the BOM is unclear, sourcing and production planning cannot move cleanly.

Typical BOM-related lead time risks include:

  • long-lead ICs are found too late
  • shortage parts need customer approval
  • package mismatch requires footprint confirmation
  • incoming PCB or component issues require rework or replenishment
  • test method is missing, so fixture or programming preparation is delayed
  • BOM revision changes after purchasing has started
  • kitting cannot be completed because one critical part is not ready

For delivery control, the useful question is not only “How many days is the lead time?” Buyers should also ask how the supplier tracks material readiness, PCB incoming quality, SMT line timing, planned warehouse date, and WIP exceptions.

At EBest Circuit, BOM review is connected with component sourcing, PCB fabrication status, SMT/THT production planning, and testing preparation. This helps reduce last-minute surprises, especially for prototype validation, small-batch builds, and repeat PCBA orders.
PCB BOM management
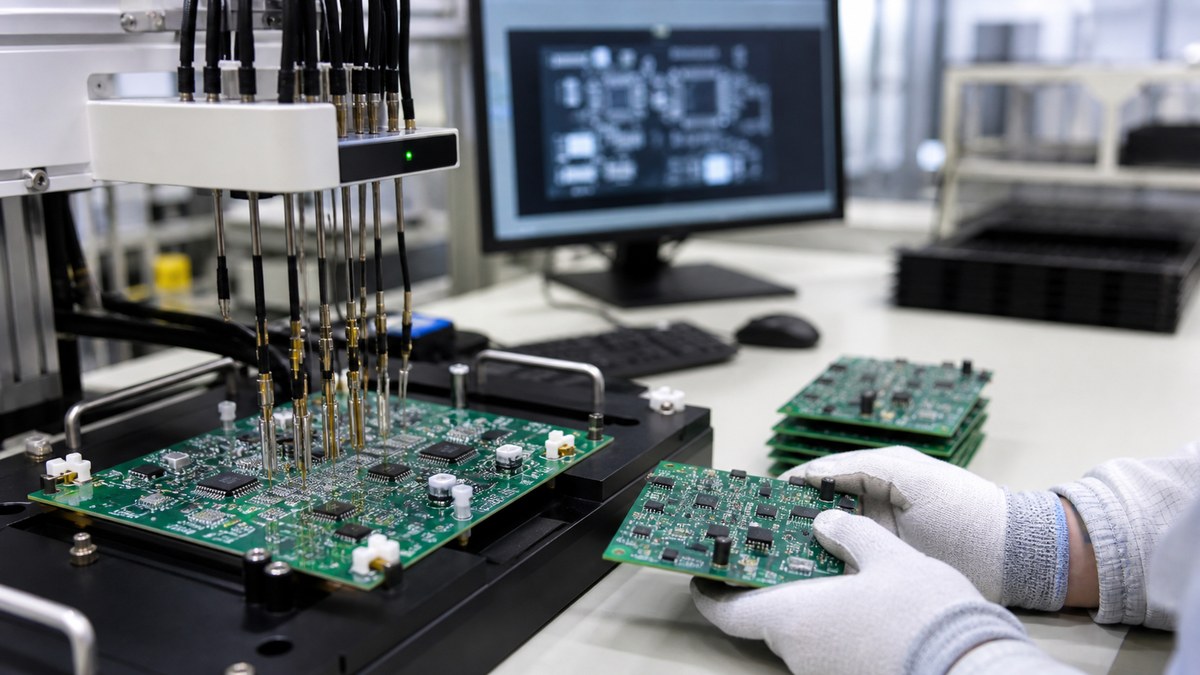
Controlled PCBA production links BOM data with assembly preparation, inspection, and testing support.

BOM Version Control for Repeat Orders

Repeat orders should be easier than first builds, but only if the BOM version is controlled. If the first order used emergency substitutes, verbal approvals, or scattered email notes, the repeat order can become another new project.

A controlled repeat-order BOM should answer:

  • Which BOM revision was actually built last time?
  • Were any temporary alternatives used?
  • Did the customer approve those alternatives for future orders?
  • Did the assembly drawing, CPL, and test requirement change?
  • Were any SMT program, stencil, fixture, or inspection notes updated?
  • Were first article or production issues recorded for the next batch?

Repeatability depends on more than placing the same PO again. SMT program records, MES process maintenance, component library data, first article confirmation, and production notes all help the next order run with fewer questions.

Traceable production records make repeat orders easier to manage. MES-based process tracking can connect BOM version, material status, production steps, inspection records, and shipment follow-up, so the next batch does not depend only on scattered emails or manual notes.

For buyers with active boards in continuous production, this is often the point that decides supplier fit. They do not want every reorder to become another sourcing project for design engineers. They want approved records, clear responsibility, and a supplier who can flag BOM risk before the next order is already late.

PCB BOM Management Case Study at EBest Circuit

A customer sent EBest Circuit a 4-layer industrial control PCBA project for a pilot run of 120 pieces. The order looked simple at first: FR4 PCB fabrication, SMT assembly, several through-hole connectors, and functional testing after assembly.

Project requirements:

  • PCB: 4-layer FR4 board
  • Quantity: 120 PCBAs for pilot validation
  • Assembly: SMT plus through-hole connectors
  • Components: MCU, power ICs, relays, terminal blocks, LEDs, resistors, capacitors, and connectors
  • Testing: power-on check and customer-defined functional test
  • Goal: validate the build before repeat production

During BOM review, several issues were found before purchasing:

  • two BOM lines used supplier codes instead of full manufacturer part numbers
  • one connector footprint needed datasheet confirmation
  • several polarized components needed clearer orientation marks
  • one relay had a longer sourcing lead time than expected
  • two ICs had possible shortage risk
  • the test method did not define pass/fail voltage limits

Before the repeat batch, one control IC moved to a long lead time. Instead of waiting for the shortage to stop production, EBest Circuit checked available alternatives, compared package and key electrical requirements, prepared sourcing information, and returned the option to the customer for approval before purchasing.

EBest Circuit solution:

  • reviewed Gerber, BOM, CPL, and assembly drawing together
  • returned BOM questions before component purchasing
  • checked connector footprint against the datasheet
  • confirmed polarity and orientation before SMT programming
  • listed sourcing options for risky ICs under customer approval
  • aligned purchasing, production material list, and assembly preparation
  • confirmed testing points before the pilot build
  • recorded approved decisions for the repeat order

Result:

The buyer received a clearer quotation and a more controlled pilot build. More importantly, the project files became cleaner for the next repeat order. Instead of treating BOM problems as isolated purchasing questions, the project was reviewed as a full PCBA build: PCB, BOM, sourcing, assembly, inspection, testing, and repeat production.

EBest Circuit BOM-to-PCBA Production Support

EBest Circuit (Best Technology) is a China-based PCB and PCBA manufacturer founded in 2006. We support buyers who need PCB fabrication, BOM review, component sourcing, SMT assembly, through-hole assembly, mixed assembly, inspection, testing support, and repeat-order follow-up.

Our support is useful when a buyer wants one team to connect BOM details with real production requirements. We do not just receive a spreadsheet and purchase parts blindly. Before production, the project team can review BOM details, Gerber files, CPL data, assembly drawings, stencil needs, tooling or fixture requirements, SMT program preparation, test requirements, and special production notes.

For production control, BOM review can also be connected with material verification, warehouse records, MES process tracking, inspection sheets, and testing preparation. This helps buyers see that BOM management is not separate from the factory floor. It is part of how the order moves from file review to purchasing, kitting, assembly, inspection, and delivery.

EBest Circuit provides customized PCB and PCBA support across:

  • FR4 PCB
  • multilayer PCB
  • metal core PCB
  • ceramic PCB
  • flexible and rigid-flex PCB
  • high-frequency PCB
  • special PCB
  • SMT PCBA
  • through-hole PCBA
  • mixed assembly
  • component sourcing
  • PCBA testing support

With more than 20 years of PCB/PCBA experience, about 260,000 square feet of monthly PCB capacity, and more than 1,000 different board types completed each month, EBest Circuit can support prototype validation, small-batch orders, and repeat production projects.

For buyers, the value is not only “BOM checking.” The value is having a manufacturing partner who can connect RFQ review, sourcing risk, approved alternatives, material kitting, SMT/THT assembly, testing preparation, and repeat-order records into one controlled production path.

FAQs About PCB BOM Management

What is PCB BOM management?

PCB BOM management is the process of keeping the PCB bill of materials accurate, approved, sourced, and aligned with the assembly files before PCBA production. It helps prevent wrong-part purchasing, quotation changes, production delays, and repeat-order confusion.

Why does a BOM affect PCBA quotation?

A BOM affects PCBA quotation because component price, package, availability, MOQ, approved alternatives, assembly difficulty, and testing scope all influence the final cost. An incomplete BOM may lead to a quote that changes after sourcing starts.

Can a supplier replace parts in my BOM?

A supplier can suggest alternatives, but the customer should approve replacement parts before purchasing or production. This is especially important for ICs, connectors, relays, sensors, power components, and any part with electrical, mechanical, or certification requirements.

Should BOM risk be checked between repeat orders?

Yes. For recurring PCBA production, BOM risk should be reviewed between orders when possible. EOL, NRND, shortage, long-lead, and approved alternative status can change before the next PO is placed.

What files should be checked together with the BOM?

The BOM should be checked with Gerber files, CPL or pick-and-place data, assembly drawings, schematics when available, test requirements, and any special production notes. These files should match the same project revision.

In Conclusion, PCB BOM management helps buyers control PCBA cost, sourcing risk, lead time, assembly quality, and repeat production stability before the order reaches the line. If you need a PCB and PCBA manufacturer to review your BOM, Gerber, CPL, assembly notes, component risks, and testing requirements before production, contact EBest Circuit at sales@bestpcbs.com.
You may also like

How to Choose Electronic Components for PCB Design?
Thursday, August 6th, 2026

For an electronic components PCB project, choose parts by translating product requirements into electrical, thermal, mechanical, manufacturing, and supply-chain limits. The right part must perform its circuit function, fit a verified land pattern, survive the real environment, remain sourceable, and pass prototype and production validation. A part number is acceptable only when every one of those conditions is documented.

Do not begin by searching for the cheapest IC or the smallest package. Begin with a requirements sheet, select the main functional devices, derive their support circuits from current manufacturer documents, and then evaluate ratings, package constraints, availability, and verification evidence. The following sequence keeps component decisions connected to PCB layout and PCBA production instead of treating the BOM as a purchasing list created after design.

Electronic Components PCB selection workbench with an assembled circuit board and organized component trays

What Requirements Should You Define Before Choosing Electronic Components for PCB Design?

Define the operating envelope before selecting any manufacturer part number. A concise component requirements sheet should state what the circuit must do and the conditions under which it must do it. Without this baseline, a component can look suitable in a parametric search while failing on startup current, logic compatibility, enclosure temperature, lifetime, or assembly constraints.

Requirement Area Questions to Resolve Component Decision Affected
Function and interfaces What must be sensed, processed, switched, stored, driven, or communicated? Main IC, analog front end, driver, memory, protection, and connector family
Power What are the nominal, startup, transient, fault, and sleep conditions? Regulators, MOSFETs, diodes, inductors, capacitors, fuses, and current-sense parts
Environment What are the ambient temperature, humidity, vibration, contamination, and altitude limits? Temperature grade, package, sealing, corrosion risk, creepage, and coating compatibility
Mechanical envelope What are the board outline, height limits, connector positions, mounting loads, and service needs? Package height, connector style, retention, heatsink, and keepout requirements
Production What volume, assembly process, inspection method, and repair strategy will be used? Package pitch, termination visibility, tape-and-reel option, moisture sensitivity, and test access
Compliance and lifetime Which market, safety, substance, automotive, industrial, or customer requirements apply? Qualification grade, declarations, traceability, lifecycle status, and approved sources

Rank each requirement as mandatory, target, or optional. Also record the source of the value: system specification, interface standard, safety analysis, mechanical model, test requirement, or customer contract. This prevents a desirable feature from being mistaken for a release condition and gives reviewers a clear reason for accepting or rejecting a candidate.

How Do You Select the Main Electronic Components for the Required PCB Function?

Select the architecture first and the exact orderable device second. The main IC must cover the required function with enough processing, interfaces, analog performance, memory, protection, and power capability, but unused features add cost, power, routing difficulty, and software risk.

  • Match the essential function: List required channels, resolution, bandwidth, timing, memory, communication interfaces, and control features before comparing product families.
  • Check system compatibility: Confirm supply rails, input thresholds, output drive, clocking, startup state, reset behavior, and communication voltage levels.
  • Assess implementation burden: Include firmware maturity, programming tools, reference software, external memory, calibration, and required analog support.
  • Compare usable packages: A device available only in a package that cannot be routed, inspected, reworked, or thermally managed is not a practical choice.
  • Evaluate failure behavior: Determine what happens during undervoltage, overcurrent, loss of communication, overheating, open sensors, and shorted loads.

A functional block diagram is useful at this stage. Assign one owner component to each major block, then record the assumptions that connect the blocks. This exposes missing level translators, isolation, protection, clock sources, interface transceivers, and power rails before the schematic becomes difficult to change.

How Do Datasheets Define the Support Components Around a Main PCB Device?

Use the current datasheet, reference design, and application notes to build each support network. Do not copy only the typical application drawing: check the surrounding equations, operating conditions, layout notes, component tolerances, and package-specific requirements.

For a power converter, calculate the inductor, input and output capacitors, feedback network, compensation, diode or synchronous switch requirements, current sense, and thermal loss using the actual input range and load profile. For a processor, review every supply domain, decoupling group, reset and boot pins, crystal or clock network, programming interface, pull resistors, and unused-pin instructions. Manufacturer guidance may also make placement part of the electrical requirement; for example, high-frequency decoupling capacitors often need a very short connection to the pin and return path.

  1. Freeze the document revision: Record the datasheet revision, errata, application notes, package drawing, and reference design used for selection.
  2. Extract mandatory networks: Separate required components from optional performance-tuning or evaluation-board features.
  3. Recalculate for the application: Replace example voltages, currents, frequency, temperature, and load assumptions with project values.
  4. Transfer layout constraints: Add placement, loop-area, grounding, thermal-via, and routing requirements to the PCB design rules.
  5. Record validation items: Identify values that must be tuned or confirmed during prototype measurement.

Which Electrical Ratings and Tolerances Matter for PCB Component Selection?

Compare worst-case circuit stress with the component’s guaranteed operating limits, not just its headline rating. Absolute maximum ratings describe a damage boundary, not a recommended continuous operating point. Use the recommended operating range and verified application conditions for normal design.

Component Parameters to Check Often-Missed Effect
Resistor Resistance, tolerance, rated power, working voltage, pulse rating, TCR A small resistor may meet average power but fail a startup or surge pulse
MLCC Capacitance, tolerance, voltage, dielectric, temperature range, ESR Effective capacitance can fall under DC bias, temperature, and aging
Inductor Inductance, tolerance, saturation current, RMS current, DCR, self-resonant frequency Peak current can cause saturation before average-current heating becomes excessive
Diode Reverse voltage, forward current, surge current, forward drop, leakage, recovery Leakage and reverse recovery can dominate high-temperature or switching behavior
MOSFET VDS, ID, RDS(on) at actual gate voltage, gate charge, SOA, thermal resistance A headline current rating may assume a thermal condition unavailable on the real PCB
IC Supply range, I/O limits, accuracy, timing, power, junction temperature Electrical performance may be guaranteed over a narrower range than basic operation
Connector Current per contact, voltage, contact resistance, cycles, wire size, temperature rise Total current and adjacent loaded contacts can reduce usable current per pin

Use worst-case analysis for tolerance stacks. A divider, filter, oscillator, current limit, feedback loop, and sensor channel can all fail even though every nominal value appears correct. For capacitors, use the manufacturer’s effective-capacitance data at applied voltage and temperature; a power-supply design that needs 10 µF cannot assume that a part marked 10 µF provides that value in circuit.

How Do Derating, Temperature, and Environment Affect Electronic Components?

Derating must follow the real stress mechanism and the component manufacturer’s conditions. A single blanket percentage is not valid for every resistor, capacitor, semiconductor, connector, or application. Establish maximum circuit stress, include tolerances and transients, calculate temperature rise, and then apply the project reliability policy.

Thermal analysis must connect the component package to the board. Power dissipation, copper area, thermal vias, airflow, neighboring heat sources, enclosure temperature, and duty cycle determine junction or hot-spot temperature. Manufacturer thermal parameters are tied to stated test boards and conditions; they are not universal package constants.

Environmental selection also covers humidity, condensation, corrosive gases, salt, vibration, shock, UV exposure, cleaning chemistry, and conformal-coating compatibility. Temperature grade alone does not prove that a device, termination finish, connector seal, or solder joint is suitable for the complete environment.

How Do PCB Component Packages, Footprints, Pinouts, and Assembly Processes Affect Selection?

A component is not PCB-ready until its exact package code and land pattern have been verified together. Similar family names can hide differences in body size, pitch, exposed pad, pin numbering, lead finish, package height, or thermal behavior.

  • Verify the package drawing: Match the orderable suffix to the manufacturer’s outline drawing, pin-one marker, terminal dimensions, pitch, coplanarity, and exposed-pad definition.
  • Build the land pattern deliberately: Use manufacturer and applicable IPC guidance, then adapt solder-mask, paste, courtyard, and via rules to the assembler’s process capability.
  • Check assembly access: Confirm pick-and-place packaging, nozzle access, component clearance, polarity visibility, AOI view, X-ray need, rework access, and hand-solder limitations.
  • Review moisture handling: Record moisture-sensitivity and floor-life controls for packages that require dry storage or baking decisions.
  • Test the library model: Compare symbol pins, footprint pads, 3D model, courtyard, and BOM package field against the same manufacturer document.

Fine-pitch and bottom-terminated packages can reduce area and electrical parasitics, but they increase stencil, voiding, X-ray, routing, and rework demands. NXP’s package guidance, for example, treats land pattern, solder mask, paste, vias, thermal transfer, and assembly as a connected system rather than independent library fields. The decision should therefore involve both PCB layout and the intended assembly process.

How Do Signal Integrity, Power Integrity, and EMC Affect PCB Component Selection?

Choose components using the electrical behavior of the complete interconnect, not isolated datasheet functions. Edge rate, impedance, parasitics, return-path continuity, loop area, current slew, and placement can make two functionally similar parts behave differently on the PCB.

For high-speed interfaces, check actual I/O standards, rise and fall times, output drive options, termination needs, package escape, clock jitter, connector bandwidth, and protection-device capacitance. For power integrity, check load transients, regulator control response, capacitor impedance versus frequency, bias-reduced capacitance, plane resistance, and anti-resonance risk. For EMC, select protection and filtering parts whose voltage, energy, current, capacitance, leakage, and frequency behavior fit both the interface and the expected disturbance.

Placement-sensitive components belong in the same decision as the main device. A decoupling capacitor with a suitable nominal value but excessive connection inductance may not suppress high-frequency current demand. Likewise, a TVS diode with excessive capacitance can degrade a fast data link even if its surge rating is adequate.

Which Reliability, Compliance, and Quality Requirements Apply to PCB Components?

Translate product-level obligations into component-level evidence before approving the BOM. Required evidence may include temperature grade, qualification status, material declarations, flammability information, traceability, change-notification support, and customer-specific approval.

Qualification labels must be read precisely. An IC qualified to AEC-Q100 is not the same as a complete automotive product approval. Confirm the exact part number, qualification revision, temperature grade, manufacturing site coverage, and applicable test group.

Similarly, assembly acceptance and soldering requirements are not substitutes for component selection. IPC identifies IPC-A-610 as an assembly acceptability standard used with J-STD-001; these documents can shape inspection requirements, but they do not prove that an electrical rating, package choice, or supplier source fits the application. Keep product compliance, component qualification, and assembly workmanship as linked but separate records.

How Does Electronic Component Selection Change from PCB Prototypes to Mass Production?

Prototype parts prove the design concept; production parts must also prove repeatability, process fit, and supply continuity. A development board, hand-soldered package, tray-packed sample, or broker-sourced device may be useful during learning but unsuitable for a controlled production release.

Decision Prototype Priority Production Priority
Availability Obtain enough parts quickly for learning Confirm authorized channels, lead time, allocation risk, and repeat-order continuity
Package May favor accessible pins or adapter boards Must match automated placement, inspection, rework, density, and thermal targets
Cost Unit price has limited impact at low quantity Evaluate total landed cost, placement cost, yield risk, inventory, and lifecycle
Testing Bench measurements and engineering access Defined programming, inspection, electrical test, functional test, and traceability
Documentation Working notes may change rapidly Released schematic, PCB, BOM, centroid, firmware, drawings, and test revision must agree

Before a pilot build, remove evaluation-only substitutions, verify reel orientation and packaging quantity, establish incoming-inspection criteria, review programming and calibration time, and freeze the design records. Feed measured prototype current, temperature, noise, startup, EMC, and tolerance results back into final ratings rather than treating a functioning bench unit as production proof.

How Should Availability, Lifecycle, Cost, and Second Sources Shape the PCB BOM?

Optimize the BOM for continuity and total production risk, not the lowest quoted unit price. Check lifecycle status, authorized availability, lead time, minimum order, packaging, price breaks, change-notification access, and realistic alternatives while the schematic can still change.

Prefer active parts with clear manufacturer support for new designs. Treat active, not recommended for new designs, last-time-buy, and obsolete as different procurement states rather than reducing them to “available” or “unavailable.” Monitor PCNs and discontinuance notices for critical devices throughout the product life.

Second sourcing is easiest for standardized passives and difficult for complex ICs, sensors, magnetics, connectors, and displays. When pin-compatible alternatives do not exist, consider footprint options, stuffing variants, or an alternate circuit architecture during design. A controlled component sourcing review should flag single-source, allocated, obsolete, unusually long-lead, or authenticity-sensitive items before production commitments are made.

How Should PCB Component Substitutes and BOM Revisions Be Controlled?

No substitute should enter production on description, package name, or pin compatibility alone. Compare form, fit, and function, then validate every parameter that can affect performance, safety, firmware, PCB layout, assembly, inspection, and sourcing.

PCB component substitutes in separate antistatic trays beside a reference circuit board and revision document
  • Confirm identity: Compare exact manufacturer part numbers, suffixes, package drawings, pinout, polarity, markings, and packing format.
  • Compare electrical limits: Review operating range, accuracy, timing, leakage, noise, transient response, protection, and worst-case tolerances.
  • Compare physical behavior: Check body and terminal dimensions, height, mass, thermal pad, solderability, MSL, and land-pattern compatibility.
  • Assess implementation impact: Identify firmware, calibration, register, boot, initialization, EMC, or test-limit changes.
  • Qualify the change: Define sample inspection, bench tests, thermal checks, functional tests, compliance regression, and pilot-build evidence proportionate to risk.
  • Release one revision: Update the approved vendor list, BOM, schematic notes, PCB variant, assembly drawing, firmware, test specification, and change record together.

Major manufacturer changes may be communicated through product change notifications when they affect form, fit, function, quality, or reliability. Treat each notice as an engineering input: identify affected products, decide whether requalification is needed, record approval, and prevent purchasing from silently mixing unapproved revisions.

How Do You Verify Electronic Components Before PCB Release?

Release the BOM only after schematic, library, procurement, manufacturing, and test evidence agree. Verification should be a documented review with named inputs and outcomes, not a final visual scan of the part numbers.

Engineer verifying PCB component packages and solder joints under a stereo microscope before release
  1. Audit requirements: Trace every critical voltage, current, timing, thermal, environmental, compliance, and lifetime requirement to a component decision.
  2. Review datasheets: Confirm current revisions, orderable suffixes, recommended operating limits, errata, support networks, and layout instructions.
  3. Validate libraries: Cross-check symbol pins, electrical types, footprint pads, pin one, exposed pads, courtyard, height, and 3D clearance.
  4. Run worst-case checks: Calculate rating margin, tolerance stacks, losses, junction temperature, startup stress, transient energy, and effective capacitance.
  5. Review DFM and DFA: Confirm the package, land pattern, solder mask, paste, spacing, orientation, inspection, X-ray, rework, and panel-process needs.
  6. Review sourcing: Check status, authorized supply, lead time, MOQ, packing, traceability, PCN access, and approved substitutes.
  7. Align release files: Ensure schematic, PCB database, BOM, approved vendor list, centroid data, assembly drawing, firmware, and test plan use the same revision.
  8. Define prototype evidence: Plan measurements for rails, current, temperature, clocks, interfaces, transients, noise, EMC pre-compliance, and functional boundaries.

The approved design database and BOM should remain the source of truth; photographs or package resemblance are not reliable substitutes. For related guidance on maintaining values, manufacturer part numbers, packages, designators, alternates, and assembly data, see the PCB parts list workflow. Revisit the electronic components PCB selection process whenever requirements, layout, firmware, supplier, or production conditions change.

FAQs About Electronic Components PCB

Q1: Should every PCB component have a manufacturer part number?

A1: Production BOM lines should specify an exact orderable manufacturer part number. Generic values may be acceptable only when the controlled procurement specification defines all permissible ratings, packages, materials, and approved manufacturers.

Q2: Can I use the absolute maximum rating as the normal design value?

A2: No; design within the recommended operating conditions. Absolute maximum ratings are damage boundaries, not intended operating points, so include tolerance, transient, thermal, and reliability margin.

Q3: Is a pin-compatible IC automatically a safe substitute?

A3: No; require a form-fit-function comparison and risk-based validation. Pin compatibility does not prove matching logic thresholds, timing, analog performance, startup behavior, thermal limits, firmware registers, package geometry, or qualification.

Q4: Should I choose the smallest available component package?

A4: The smallest package is not always the lowest-risk production choice. Use it only when routing, thermal performance, placement, inspection, rework, and supplier capability support it.

Q5: What information should an approved component record contain?

A5: The record must provide unambiguous identity and revision control. Include the exact part number, manufacturer, description, value, ratings, tolerance, package, lifecycle, declarations, approved source, datasheet revision, alternates, and approval evidence.

Q6: How many alternative components should be approved?

A6: There is no universal number of approved alternatives. Qualify them where supply risk justifies the effort; a critical single-source item may need an architectural contingency, while common passives may support multiple prequalified sources.

Q7: Can prototype components be purchased from any available seller?

A7: Prefer authorized, traceable sourcing appropriate to the product risk. Development needs do not remove authenticity risk, so document any exception and avoid using uncertain parts for qualification or production decisions.

Q8: When should component selection be frozen?

A8: Freeze the production BOM only after all release evidence agrees. Requirements, schematic, footprint, worst-case analysis, DFM, sourcing, prototype results, and test plans must align; later changes require formal engineering change control.

Q9: Does RoHS status prove that a component meets all compliance needs?

A9: No; verify each applicable compliance obligation separately. RoHS addresses restricted substances within its scope, not electrical safety, automotive qualification, EMC performance, reliability, or end-product suitability.

Q10: What files should be sent to a PCBA supplier for component review?

A10: Send a complete, revision-aligned manufacturing data set. Include the released BOM, Gerber or ODB++, centroid file, assembly drawings, schematic when permitted, substitute rules, programming requirements, and test instructions.

Conclusion

Reliable PCB component selection connects circuit performance to manufacturability, verification, and supply continuity. Define requirements first, derive support networks from current manufacturer documents, verify ratings and footprints, plan for production and lifecycle risk, and control every substitute through documented change review. EBest Circuit can support the transition from design files and BOM review to PCB fabrication and PCBA preparation without replacing the customer’s component-design authority. If you are sourcing PCB/PCBA manufacturing, send your Gerber/ODB++, BOM, quantity, stackup, assembly, programming, and test requirements to sales@bestpcbs.com for engineering review and a quotation.

You may also like