Choosing a copper core PCB supplier is rarely just about finding a factory that can make a metal-base board. Buyers usually already have a thermal-management requirement. The real decision is whether the supplier can manufacture the required copper-core structure, hold the specified material and dimensions, control quality, meet the delivery schedule, and support PCBA when the project goes beyond a bare PCB.
EBest Circuit has 20+ years of PCB and PCBA manufacturing experience, with production support in China and Vietnam and customers across 40+ countries. Our capabilities cover copper core PCB, heavy copper, HDI, rigid-flex, high-frequency PCB and downstream assembly, supported by 4 SMT lines, SPI, AOI, X-ray, ICT and functional testing. PCB fabrication, component sourcing, assembly and testing can be coordinated within one project for customers who want fewer supplier handoffs.
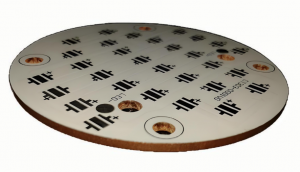
Copper-core PCB manufacturing for high-power thermal-management applications.
Top 5 Copper Core PCB Suppliers in China to Compare
China has an established copper-base PCB supply chain, but suppliers differ in ordering model, thermal structures, PCBA coverage and suitability for customized projects.
The following five companies are useful suppliers to compare rather than an absolute quality ranking.
Supplier
Best Fit
EBest Circuit
Custom copper PCB + PCBA
JLCPCB
Standard online prototypes
PCBWay
Prototype and custom builds
NextPCB
Copper-core fabrication
PCBONLINE
Multilayer and special structures
JLCPCB is attractive when the design fits a standardized online ordering model. PCBWay also serves prototype and custom PCB buyers with metal-base options. NextPCB publishes dedicated copper-core manufacturing information, while PCBONLINE covers several copper-base PCB structures.
EBest Circuit is better suited to projects that require engineering review, customized copper-core construction, material control, component sourcing, assembly or repeat production.
The useful sourcing question is not simply, “Which supplier is cheaper?”
Which copper core PCB supplier can manufacture the released design without changing the thermal, material or quality requirements that matter to the product?
What Copper Core PCB Manufacturing Capabilities Can EBest Circuit Support?
The fastest way to judge a copper core PCB supplier is to compare your released design with its actual manufacturing limits.
EBest Circuit supports standard and special metal-base PCB processes with the following production ranges:
Capability
EBest Circuit Capability
Thermal conductivity
1W, 2W, 3W; 3–8W by material confirmation
PCB structure
Single-sided, double-sided, 2-layer; special 4-layer builds
Special structure
Thermoelectric-separation copper PCB
Inner copper
0.5–3 oz standard
Outer copper
1–3 oz standard
Board thickness
0.8–3.0 mm standard; 4–5 mm by review
Min. finished PTH
0.45 mm standard; 0.30 mm by review
Max. PTH aspect ratio
6:1
Trace / space
0.20/0.20 mm standard at 1 oz; 0.15/0.15 mm by review
Outline tolerance
±0.15 mm standard; ±0.10 mm special
Surface finish
HASL, OSP, ENIG, immersion Ag/Sn, gold finger
Copper weight is especially important because the achievable trace and spacing change as copper becomes thicker. For example, our regular outer-layer capability is approximately:
1 oz: 0.20 / 0.20 mm trace/space
2 oz: 0.25 / 0.25 mm
3 oz: 0.35 / 0.35 mm
4 oz: 0.50 / 0.50 mm, subject to structure review
The thermal material also needs to be specified correctly. We regularly work with 1W, 2W and 3W thermal materials. Higher-conductivity materials in the 3–8 W/m·K range can be evaluated after material availability and construction are confirmed.
For insulation-layer construction, regular PP thickness is around 100–110 μm, while 150 μm and 200 μm options require confirmation.
These numbers give buyers a much faster answer than a generic claim such as “we manufacture copper core PCB.” If your copper weight, board thickness, thermal conductivity, hole size and line width fall within these ranges, the project can move directly into a more detailed DFM review. More demanding specifications can be evaluated against the special-process limits.
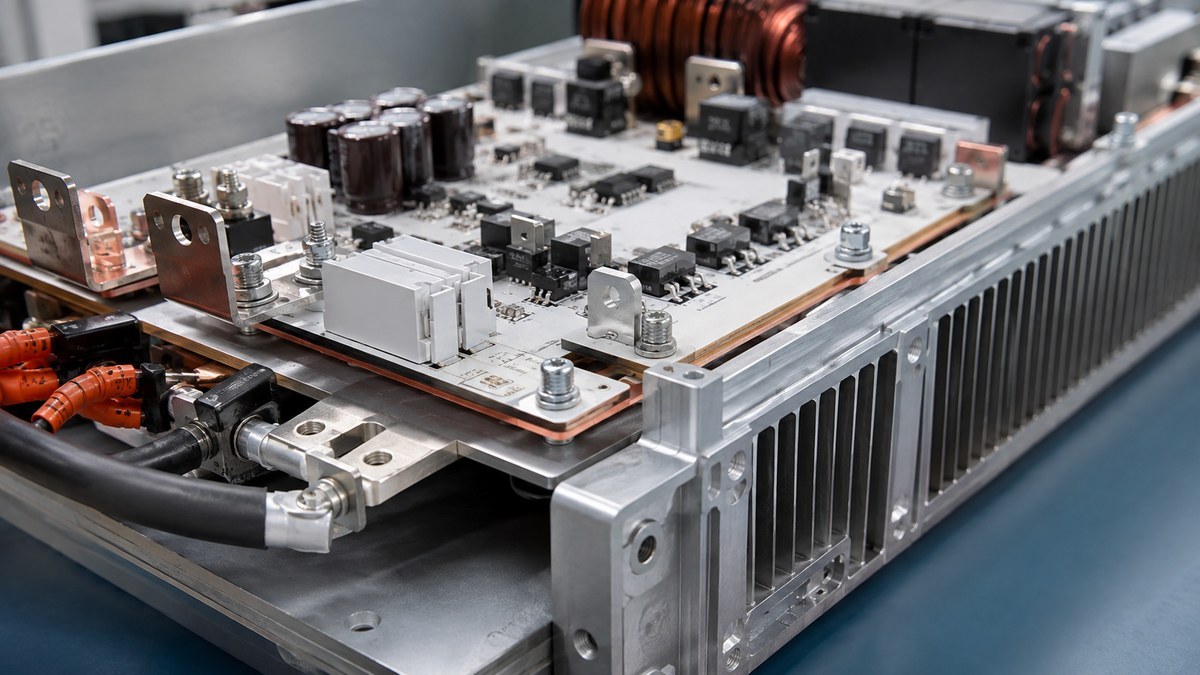
A copper-core PCB integrated with a heat spreader for power electronics.
How Is Copper Base PCB Quality Controlled Before Shipment?
Copper base PCB quality control should result in fewer insulation, dimensional, soldering and mechanical-fit problems after delivery.
At EBest Circuit, attention is focused on the areas that directly affect the finished board:
Construction consistency: copper thickness, dielectric structure and finished thickness follow the approved specification.
Electrical isolation: insulated structures must maintain separation between the circuit and metal substrate.
Hole accuracy: standard PTH diameter tolerance is ±0.075 mm, while NPTH tolerance can reach ±0.05 mm.
Mechanical fit: standard outline tolerance is ±0.15 mm, with ±0.10 mm available for qualifying requirements.
Solderability: pads, solder mask and surface finish are checked before assembly.
Electrical integrity: electrical testing helps detect opens and shorts before shipment.
When the copper core PCB continues into assembly, inspection can extend to SPI, AOI, X-ray, ICT and functional testing according to the board and acceptance requirements.
The benefit is not simply more inspection steps. It is less risk of discovering a PCB problem after higher-value components have already been mounted.
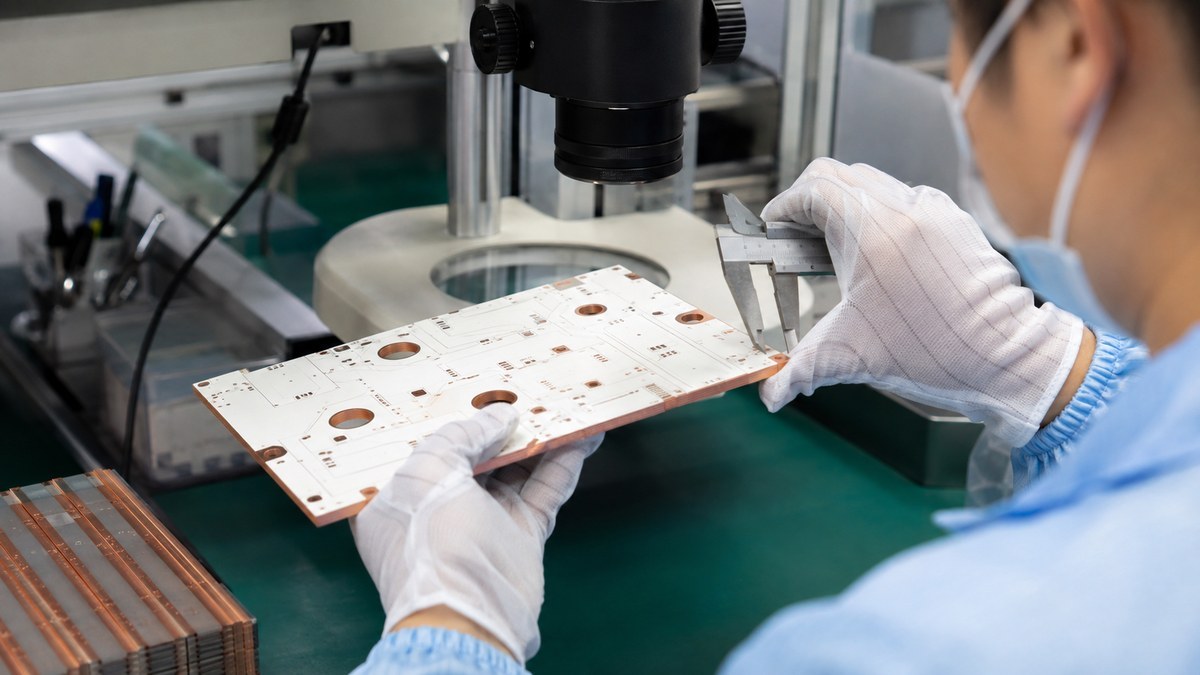
Dimensional inspection of a copper-core PCB before assembly.
Which Certifications and Standards Matter for Copper Core PCB Production?
Not every copper core PCB needs the same certification set. The relevant requirements depend mainly on the final product and the customer’s supplier-qualification rules.
Application
Common Requirement
Industrial
ISO 9001, IPC
Automotive
IATF 16949
Medical
ISO 13485
Aerospace
AS9100D
Environmental
RoHS, REACH
UL-required products
Applicable UL system
EBest Circuit supports projects under quality systems including ISO 9001, ISO 13485, IATF 16949 and AS9100D, together with applicable UL, RoHS, REACH and IPC requirements.
The important point is not to require every certificate for every board.
An automotive copper-base PCB may make IATF 16949 part of supplier qualification. A medical project may require ISO 13485, while an aerospace program may use AS9100D as a sourcing gate.
For a general industrial copper core PCB, the applicable IPC requirements, materials and customer acceptance criteria may matter more than an unnecessarily long certification list.
The right certification should qualify the manufacturing route, not simply decorate the supplier page.
How Fast Can Copper Core PCB Prototypes and Production Orders Ship?
For standard PCB builds, EBest Circuit typically plans around 3–5 working days, with expedited production available for qualifying projects.
Copper core PCB lead time may increase when the design includes:
high-conductivity material requiring special sourcing;
non-standard copper-base thickness;
multilayer construction;
thermoelectric-separation structures;
special machining;
additional testing.
For the customer, the real benefit is knowing the realistic ship date before production starts.
We consider engineering review, material readiness, fabrication, assembly and testing when estimating the schedule. A three-day fabrication cycle, for example, has little value if the specified 5 W/m·K material requires additional sourcing time.
For PCBA orders, component availability must also be included before a dependable delivery date can be confirmed.
Can a Copper Core PCB Supplier Also Handle PCBA?
Yes. For many thermal-management products, having one supplier handle both copper core PCB fabrication and assembly can simplify the project considerably.
A copper-base board may later carry LEDs, MOSFETs, power modules, connectors or other heat-generating components. Splitting these stages can leave the customer coordinating:
EBest Circuit can combine these activities within one manufacturing project.
Customers gain:
Fewer supplier handoffs: PCB, sourcing, assembly and testing can stay together.
Faster issue resolution: PCB and assembly questions are handled within the same project.
Better BOM control: turnkey, partial-turnkey and consigned sourcing are available.
Inspection matched to the build: SPI, AOI and X-ray can be applied where appropriate.
Clearer responsibility: PCB-related assembly issues do not need to be negotiated between separate factories.
This approach is particularly useful for LED lighting, power electronics, industrial control and automotive applications where the PCB and mounted devices work together as one thermal system.
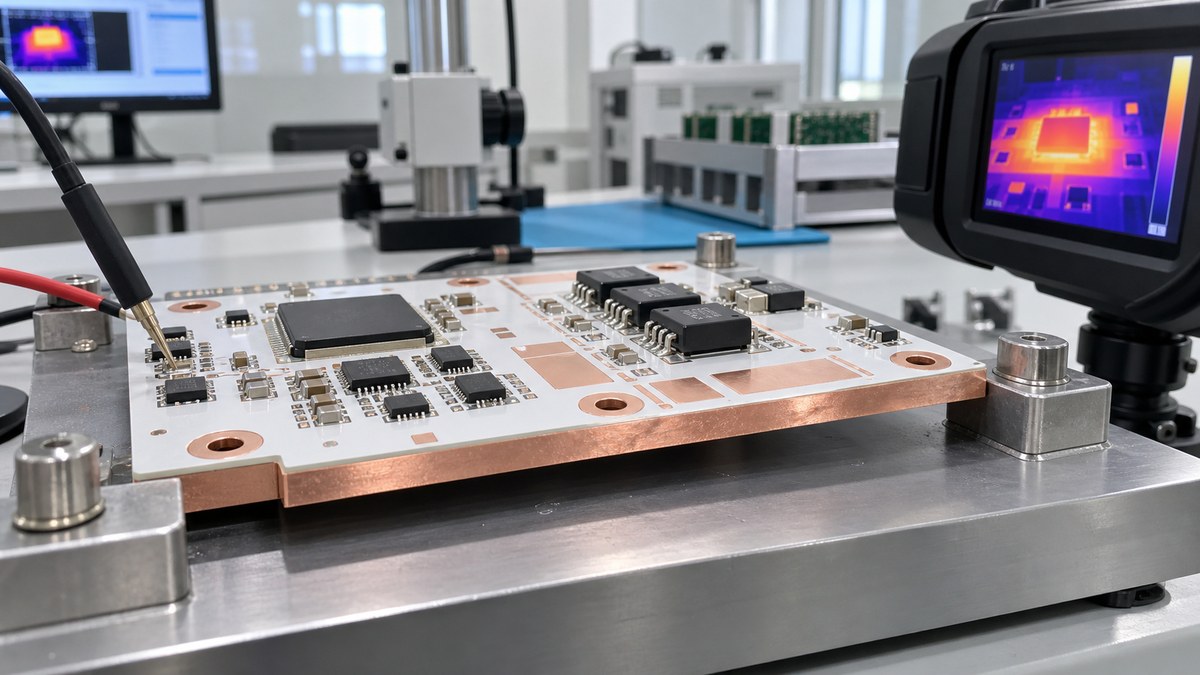
Thermal inspection of an assembled copper-core PCB with its metal core visible.
Copper Core PCB Case Study: From Thermal Design to Production
One copper-core lighting project required a 2-layer copper core PCB with downstream assembly.
Item
Specification
PCB
2-layer copper core
Thickness
1.60 mm ±10%
Circuit copper
1 oz
Thermal conductivity
3 W/m·K
Finish
OSP
Assembly
Included
Application
Pool lighting
The customer needed more than a bare copper-base board. The 3 W/m·K thermal material, 1.6 mm construction, surface finish and assembly process had to work within the same finished lighting product.
EBest Circuit coordinated PCB fabrication and PCBA within one project rather than transferring the board between separate manufacturers.
For the customer, this meant fewer supplier interfaces and one approved manufacturing package that could support repeat builds.
The project also shows why a copper core PCB should not be specified simply as “use copper.” Thermal dielectric, copper weight, board thickness, surface finish and downstream assembly all affect the finished product.
Why Choose EBest Circuit as Your Copper Core PCB Supplier?
A good copper core PCB supplier should reduce the work and risk the customer has to manage.
With EBest Circuit, buyers gain:
More design flexibility: standard and special copper-base structures can be evaluated against clearly defined process limits.
One manufacturing route: PCB fabrication, sourcing, PCBA and testing can stay within one project.
Fewer surprises before fabrication: thermal material, copper weight, thickness and assembly requirements are reviewed before release.
Better control over changes: material and component alternatives remain subject to customer approval.
Easier repeat production: approved construction and production requirements remain connected to future orders.
Broader quality-system coverage: industrial, automotive, medical and aerospace projects can be supported under relevant quality frameworks.
For international customers, the value is not simply a lower bare-board price. It is knowing what the factory can manufacture, reducing supplier handoffs and keeping responsibility clearer from copper-core PCB fabrication through finished PCBA.
Start with measurable manufacturing limits. Compare the required thermal conductivity, copper weight, board thickness, layer structure, minimum hole, trace/space, surface finish and quality requirements with the supplier’s actual production capability.
Is copper core PCB better than aluminum PCB?
Not in every application. Copper provides stronger heat spreading and can suit more demanding thermal designs, but it is heavier and usually more expensive. Aluminum remains practical for many LED and power-electronics applications where its thermal performance is sufficient.
What thermal conductivity should I specify for a copper core PCB?
Do not judge the PCB by bulk copper conductivity alone. The thermal dielectric and its thickness can strongly affect overall thermal resistance. EBest Circuit regularly supports 1W, 2W and 3W thermal materials, while 3–8 W/m·K materials can be evaluated according to availability and construction.
How thick can a copper core PCB be?
EBest Circuit’s regular metal-base PCB thickness range is 0.8–3.0 mm. Thicknesses of 4.0 mm or 5.0 mm can be evaluated when suitable material is available.
Can copper core PCBs use heavy circuit copper?
Yes. Regular inner-layer copper capability is 0.5–3 oz, while outer layers commonly support 1–3 oz. Higher copper weights require review because trace/space and etching requirements change as copper becomes thicker.
Can one copper core PCB supplier provide both fabrication and assembly?
Yes. EBest Circuit provides copper core PCB fabrication together with component sourcing, SMT/THT assembly, inspection and customer-defined testing, reducing the need to coordinate several manufacturing suppliers.
Ready to Start Your Copper Core PCB Project?
If you are preparing a copper core PCB or PCBA project, send your Gerber files, fabrication drawing, BOM, assembly requirements, and target quantity to sales@bestpcbs.com. Our engineering team can review the stackup, copper-base structure, thermal requirements, manufacturability, assembly needs, and lead time before quotation.
Choose a metal core PCB manufacturer in the USA by matching the released construction, evidence package, quantity profile, and assembly scope to the factory that will build the order. A suitable manufacturer must be able to control the specified metal base, dielectric, copper, hole isolation, mechanical features, surface finish, and assembly interface as one design.
Shortlist suppliers by project fit and order evidence. Confirm who will manufacture the board, which material and process route will be used, what records will accompany the order, and whether those controls remain stable from prototype through repeat production. This keeps the selection process focused on a manufacturable, verifiable board rather than a long list of unrelated capabilities.
What Should You Verify Before Shortlisting a Metal Core PCB Manufacturer Serving the USA?
Start with eight selection factors that determine whether a supplier can support the complete order. Remove candidates that cannot match the construction, evidence, quantity, or assembly scope before engineering time is spent on detailed quotations.
Relevant production history: Ask for evidence of work with the same MCPCB construction; standard single-sided aluminum experience does not qualify every metal-core build.
Metal-base range: Confirm the supported aluminum alloys, copper bases, thicknesses, and any special bonded or machined structures.
Thermal material control: Review dielectric grade, thickness, thermal performance, electrical isolation, and substitution policy together.
Custom construction capability: Match plated holes, multilayer bonding, pockets, routing, countersinks, and other drawing features to the proposed factory.
Order-level quality evidence: Define material, dimensional, electrical, isolation, and traceability records that will be released with the lot.
Assembly integration: If PCBA is required, check whether fabrication, soldering, heat-sink interfaces, inspection, and test ownership are coordinated.
Quantity fit: Confirm prototype support, intended production capacity, tooling, material availability, and repeat-order controls.
DFM response: A useful review identifies a specific drawing, material, isolation, machining, or assembly risk and returns a clear decision or question.
Which Metal Core PCB Construction Must the Manufacturer Prove?
Approve a supplier across the independent construction axes used by your design, because “metal core PCB” does not describe one manufacturing route. Separate the base material, circuit-layer structure, thermal-path architecture, electrical specialization, and mechanical integration before checking factory experience.
Base material axis: For aluminum, verify alloy, thickness, laminate, profiling, and panel control; for copper, add source control, weight, oxidation protection, machining, and handling.
Circuit-layer axis: A single-sided IMS route differs from a plated double-sided or multilayer route. Confirm hole isolation, bond sequence, registration, stackup limits, and internal-construction evidence as applicable.
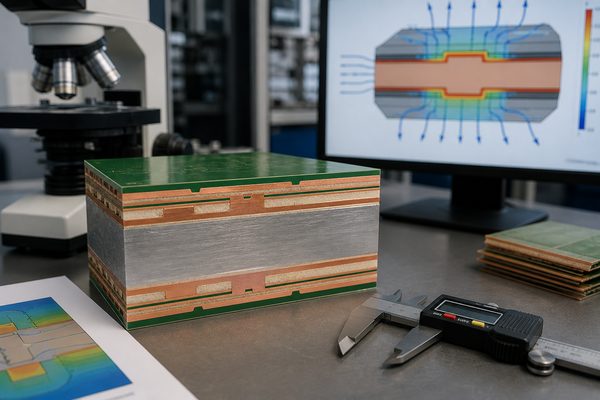
Thermal-path axis: Distinguish a conventional dielectric-based path from a direct thermal path. Require a cross-section that shows both heat flow and electrical isolation.
Electrical-specialization axis: Power and LED IMS work emphasizes thermal and assembly control, while RF metal-backed work adds RF laminate handling, bond film, pockets, metal-carrier plating, dimensional datums, and finish compatibility.
Mechanical-integration axis: Separate a standard profiled base from a precision-machined carrier. Direct mounting to a heat sink, housing, or frame brings outline, holes, flatness, burr, pocket, and mounting surfaces into supplier qualification.
A supplier experienced with single-sided LED aluminum boards may still lack the plated, multilayer, direct-path, RF, or precision-machining controls required by another design. Ask the candidate to mark each axis as routine, conditional, or outside its current process window.
Which MCPCB Specifications Should You Confirm Before Choosing a Manufacturer?
Match the required stackup to a confirmed factory process window before approving a supplier. Best Technology publishes the following reference values in its single-layer MCPCB data and current product catalog. Use them for initial quotation screening. Only a build-specific review can confirm whether the required material, copper, geometry, thickness, layer count, and panel size can be produced together.
Capability item
Best Technology reference range
What to confirm for the order
Single-layer base material
Aluminum, copper, or iron alloy
Exact alloy, metal thickness, source, surface treatment, and whether the quotation uses the named material
Single-layer dielectric conductivity
0.8, 1.0, 1.5, 2.0, or 3.0 W/(m·K)
Material manufacturer and grade, dielectric thickness, thermal resistance, dielectric strength, and substitution rule
Copper weight
0.5, 1.0, 2.0, or 3.0 oz; up to 10 oz is listed
Finished copper, minimum line/space at that weight, etching tolerance, and inspection method
Single-layer board thickness
0.5–3.0 mm
Finished-thickness tolerance, flatness, mounting interface, and panel handling
General MCPCB layer count
1–10 layers
Released cross-section, plated-hole isolation, lamination sequence, registration, and factory history with that structure
General MCPCB board thickness
0.8–5.0 mm
Whether the requested thickness is valid with the selected layer count, metal base, copper, machining, and panel size
Minimum line/space
4/4 mil, or 0.10/0.10 mm
Applicable copper weight, conductor tolerance, annular features, and production inspection basis
Send the same drawing, cross-section, quantities, and evidence requirements to every shortlisted supplier. Require the quotation to identify which values are routine, which require engineering review, and which combinations are unavailable at the named factory.
How Do You Verify the Manufacturer’s Quality and Traceability?
Reliability is demonstrated when the supplier can connect its quality system to your material, revision, lot, tests, and changes. Verify the certificate’s legal entity, site, and scope, then require order-specific material, revision, lot, test, and change records.
Site and scope: Check the legal entity, factory address, certificate scope, and actual operations used for the proposed order.
Incoming materials: Confirm how the metal base, thermal laminate, copper, solder mask, and finish materials are identified and released.
Process traceability: Ask how work orders, material lots, inspection results, deviations, and final shipments remain linked.
Electrical controls: Define the net test and any isolation requirement with the test method, voltage or limit supplied by the approved specification.
Dimensional controls: Identify which holes, cutouts, thicknesses, flatness points, and datums receive recorded inspection.
Nonconformance handling: Require segregation, disposition authority, corrective action, and customer notification for deviations that affect fit or performance.
Change control: Specify which material, process, factory, tooling, or sub-supplier changes require approval before the next lot.
The useful output is a qualification record that states what was verified, what remains conditional, and which documents will be delivered with production. Avoid approving a supplier from a logo sheet or questionnaire that is not connected to the actual build route.
How Do Material and Thermal Controls Affect Supplier Qualification?
Select a manufacturer whose routine materials and process controls match the metal base already justified by the thermal, mechanical, electrical, and cost design. Material selection comes first; supplier qualification then verifies the factory controls needed for that base and construction.
For an aluminum PCB project
Material identity: Confirm the base alloy, thickness, approved thermal laminate, dielectric thickness, and substitution limits.
Profiling control: Review routing, punching where applicable, V-scoring, burr control, and panel-to-board flatness.
Repeatability: Ask how thermal material and base-metal lots are controlled across prototype and production orders.
For a copper core PCB project
Base handling: Confirm copper-base weight, sourcing, oxidation protection, machining, and in-process handling.
Construction complexity: Review bonding, direct-path features, plated isolation, pockets, and registration with a cross-section.
Commercial impact: Ask the supplier to separate material, machining, tooling, yield-sensitive features, and assembly costs in the quote.
Do not assume that a high-volume aluminum IMS line can automatically produce a copper pedestal, plated metal-core, or RF metal-backed design. Qualification follows the released structure, not the broad MCPCB category.
Which Thermal Material Records Should the Supplier Provide?
Thermal material must be compared as a system because conductivity alone does not define heat flow or insulation performance. Two laminates with the same nominal W/m-K value can use different dielectric thicknesses and therefore produce different thermal resistance and electrical margins.
Thermal conductivity: Record the published value, test basis, and grade instead of accepting an unlabeled number.
Dielectric thickness: Confirm the finished or nominal thickness used in the thermal and isolation assessment.
Thermal resistance: Compare the full dielectric path and relevant area instead of using the material conductivity headline by itself.
Dielectric strength: Tie the required electrical isolation to an approved test method and design margin.
Material identity: Lock the manufacturer, grade, and accepted equivalent route when consistency matters.
Substitution policy: Require approval before a supplier changes grade, thickness, or source, even if the nominal conductivity is unchanged.
A strong candidate can return an approved stackup or material proposal that shows the copper, dielectric, and metal-base relationship. A weak candidate quotes “2 W/m-K” or “3 W/m-K” without naming the grade, dielectric thickness, isolation basis, or substitution boundary.
Can the Manufacturer Control Both Mechanical Fit and PCB Assembly?
Mechanical capability can disqualify an otherwise suitable MCPCB supplier when the board mounts directly to a heat sink, housing, or structural frame. Control the metal base as both a precision interface and a thermal layer.
Outline and datums: Define the dimensions that locate the board in the final assembly and the datum scheme used for inspection.
Slots and cutouts: State size, position, corner-radius, and burr requirements that affect clearance or fit.
Countersinks and countersunk holes: Specify side, angle, final diameter, depth, plating status, and relationship to the mounting hardware.
Routing and V-scoring: Confirm the separation method, residual thickness where relevant, edge quality, and component-to-edge constraints.
Flatness: Define the measurement condition and acceptance limit for the bare board or assembled board, whichever controls fit.
Mounting holes: Identify electrical isolation, annular clearance, tolerance, and any metal exposure requirement.
Surface contact: Mark heat-sink interfaces, keep-out areas, thermal interface material, and cosmetic or conductive surfaces on the drawing.
Ask the supplier which features are measured, with what fixture or datum, and whether the result is recorded. A drawing that says “fit to heat sink” without measurable criteria cannot produce a comparable supplier decision.
How Should Assembly Capability Be Verified?
Choose an assembly-capable manufacturer when fabrication choices and the soldering or mounting process share the same thermal and mechanical risks. The evaluation should connect the bare-board design to component placement, reflow, heat spreading, attachment, and test access.
High-power components: Review pad geometry, copper spreading, void-sensitive thermal pads, component limits, and inspection access for LEDs, MOSFETs, IGBTs, or similar devices.
Soldering process: Confirm the assembly profile is compatible with the laminate, finish, board mass, component set, and approved materials.
Heavy components: Check support, handling, depaneling, connector loads, and any secondary mechanical attachment.
Thermal interface: Define the heat sink, interface material, mounting hardware, torque source, cleanliness, and flatness assumptions when they are part of the order.
Inspection plan: Select AOI, X-ray, solder-joint inspection, or other methods only where the component and joint geometry make them useful.
Test ownership: State whether the supplier performs bare-board electrical testing, assembly inspection, programming, functional testing, or customer-defined verification.
If fabrication and assembly are split between suppliers, assign responsibility for material storage, solder-profile approval, thermal interface preparation, board damage, and failure analysis. The lowest bare-board price can lose value when those interfaces are unmanaged.
Which Tests Should Be Included in the Manufacturer’s Release Package?
The test package should verify the risks created by the released construction and drawing. Not every order requires every test, so define the method, sample or lot coverage, acceptance basis, and record before comparing suppliers.
Electrical test: Verify opens and shorts against the released net data using the agreed coverage and acceptance rules.
Isolation test: Apply the approved method where conductors, plated holes, mounting features, or direct-path structures must remain isolated from the metal base.
AOI: Use image inspection for applicable conductor, pad, and solder-mask features while recognizing that it does not replace electrical or internal construction evidence.
Dimensional inspection: Record critical outlines, holes, slots, countersinks, thicknesses, and datums that control assembly fit.
Flatness inspection: Define support condition, board state, measurement points, and limit before treating a result as comparable.
Material verification: Link the approved dielectric and metal base to the received lot and production traveler.
Microsection: Use it when plated, bonded, multilayer, or isolation features require internal construction evidence.
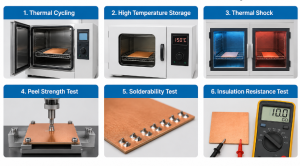
Solderability or finish evidence: Specify it when shelf life, assembly process, contact use, or a customer requirement makes the result relevant.
For any temperature or thermal comparison, define input power, sensor position, ambient condition, heat sink, thermal interface material, mounting force, stabilization time, and board revision. Results measured under different conditions should not be used to rank suppliers.
Can the Manufacturer Maintain the Same Controls from Prototype to Volume?
A prototype supplier is suitable for volume only when the intended factory, material route, tooling, controls, and change process can scale with the order. Treat a successful sample as evidence for that build only; volume approval requires the intended production route and repeat-order controls.
Prototype objective: Close DFM questions and verify thermal, electrical, mechanical, assembly, and test interfaces before the design is frozen.
Material availability: Identify whether the prototype uses stocked material, a temporary substitute, or the intended production grade.
Tooling route: Record temporary and production tooling differences for profiling, fixtures, stencils, inspection, and test.
Pilot evidence: Use the intended process route and review representative material, dimensional, electrical, isolation, and assembly records.
Production release: Freeze the approved data, factory, material, substitution limits, test scope, packaging, and change-notification rules.
Repeat-order control: Compare each new lot against the released revision and approved deviations rather than relying on the previous purchase order alone.
Ask who owns the transfer from engineering samples to production and what must be requalified if the factory, material, tooling, or assembly route changes. This answer is often more useful than a broad annual-capacity figure.
How Should You Compare Quotes from MCPCB Manufacturers Serving the USA?
Compare price only after every supplier has quoted the same construction, quantity, evidence, responsibility, and delivery basis. Otherwise, a lower total may reflect a thinner dielectric, different metal base, relaxed tolerance, reduced testing, excluded tooling, or a different assembly scope.
Quote field
Equal-scope check
Materials
Same dielectric grade or approved equivalent, thickness, conductivity basis, metal type, and base thickness
Copper and stackup
Same copper weights, layer construction, finished thickness, and plated or isolated features
Mechanical scope
Same outline, slots, holes, countersinks, flatness, burr, tolerances, and tooling assumptions
Finish and marking
Same surface finish, solder mask, legend, exposed metal treatment, and packaging requirements
Inspection and tests
Same electrical, isolation, dimensional, construction, assembly, and reporting scope
Assembly responsibility
Same component sourcing, stencil, placement, soldering, inspection, programming, functional test, and rework boundary
Commercial basis
Same quantity, tooling treatment, delivery point, freight, duties, payment terms, and production site
Use one comparison sheet for every metal core PCB manufacturer in the USA that reaches the final shortlist. Mark assumptions and exclusions explicitly, then ask each supplier to close the gaps before the commercial decision.
Which Supplier Red Flags Should Stop or Delay Approval?
Reject or hold a supplier when its quote hides the material, process, evidence, or change boundary that controls your design. Each red flag below creates a specific downstream risk.
No material grade: A quote that says only “aluminum PCB” or “3 W/m-K” permits unknown dielectric identity and inconsistent substitutions.
Conductivity without thickness: The thermal path cannot be compared when dielectric thickness and thermal resistance are missing.
No hole-isolation answer: Plated or mounting features near the metal base may create electrical failure or an unbuildable stackup.
Unexplained low price: A large price difference may come from different materials, tolerances, testing, tooling, production sites, or excluded services.
Prototype-to-volume material change: The approved sample may not represent the production board if grade or supplier changes are uncontrolled.
Undefined test scope: “100% tested” has little value without naming the test, coverage, method, limit, and record.
No traceability: Material, traveler, test, and shipment records cannot support containment or root-cause analysis when lots are not linked.
No DFM response to unusual features: Silence on countersinks, pockets, isolated holes, tight flatness, or thermal-interface details may indicate that the supplier has not reviewed the actual construction.
Do not treat one red flag as an automatic rejection when the supplier can clarify and document the point. The decision should record the closed answer, any approved exception, and the evidence required before production release.
What Should a USA-Bound MCPCB RFQ Include?
A quote-ready package must define the electrical data, stackup, thermal material, mechanical interface, quantity, assembly scope, and evidence expectations. Sending this information together reduces assumptions and makes supplier responses comparable.
Electrical fabrication data: Gerber or ODB++, NC drill files, netlist where available, board revision, and fabrication drawing.
Cross-section: Copper weights, dielectric grade and thickness, metal type and thickness, finished thickness, and layer sequence.
Thermal and isolation requirements: Thermal property basis, dielectric strength or isolation requirement, direct-path details, and approved test conditions.
Finish and marking: Surface finish, solder mask, legend, exposed metal surfaces, special cleanliness, and packaging needs.
Order profile: Prototype quantity, pilot quantity, volume forecast, delivery location, requested production site, and trade terms.
Assembly data: BOM, pick-and-place file, assembly drawing, approved component alternatives, stencil or soldering constraints, and heat-sink interface details.
Verification package: Required electrical, isolation, dimensional, construction, assembly, programming, functional-test, traceability, and change records.
Send the controlled package to sales@bestpcbs.com and request a free DFM review plus a quotation that states the proposed material, construction, open questions, inspection scope, assembly responsibility, and delivery basis.
Why Choose EBest Circuit for USA-Bound Metal Core PCB Projects?
EBest Circuit gives US buyers one engineering and commercial interface for metal-core fabrication, assembly planning, inspection scope, and repeat-order control. EBest is a China-based source manufacturer, so every quotation should identify the manufacturing origin, proposed construction, evidence package, and delivery basis clearly.
Construction-specific review: Aluminum, copper-base, plated, multilayer, direct-path, and machined structures are reviewed against the released cross-section and drawing.
Published capability references: The supplier can begin with concrete material, conductivity, copper, thickness, geometry, and size values, then identify which combinations require engineering review.
Free DFM review: Drilling, hole isolation, routing, machining, flatness, thermal-interface, and assembly questions can be closed before quotation release.
PCB and PCBA coordination: Fabrication, component sourcing, SMT/THT assembly, inspection, and project-specific test responsibilities can be defined in one order scope.
Prototype-to-production control: Material identity, drawing revision, approved deviations, inspection requirements, and change-notification rules can remain linked to repeat orders.
Quote transparency: The quotation can state assumptions, exclusions, tooling, evidence, assembly responsibility, manufacturing site, and delivery terms for an equal-scope comparison.
Send the controlled design package to sales@bestpcbs.com for a construction review and a quote that identifies open technical decisions before production.
FAQs About Selecting a Metal Core PCB Manufacturer for the USA
Q1: Does a US sales office mean the board will be manufactured in the USA?
A1: No. Ask for the physical factory address and the operations performed there, including imaging, etching, drilling, bonding, profiling, finish, and electrical test where relevant. Put any country-of-manufacture requirement in the RFQ, supplier response, and purchase documentation so the order does not depend on a sales-address assumption.
Q2: Should I ask for a sample before approving an MCPCB supplier?
A2: Use a sample that represents the intended material and process route. A generic sample may show workmanship, but it does not qualify your dielectric, metal base, isolation, machining, or assembly interface. Record which features the sample proves and which items still require first-article or pilot evidence.
Q3: Can a supplier substitute a thermal laminate with the same W/m-K rating?
A3: Only after technical review and approval. Check dielectric thickness, thermal resistance, dielectric strength, adhesion, assembly compatibility, availability, and change records before accepting an equivalent. Require the supplier to identify the proposed grade and explain which released requirements remain unchanged instead of approving it from conductivity alone.
Q4: When should I request a microsection?
A4: Request one when internal construction evidence affects release. Plated holes, multilayer bonding, isolated features, or a customer requirement may justify a representative microsection. Define the sampled feature, lot or panel relationship, preparation method, acceptance basis, and record retention before treating the image as production evidence.
Q5: Is an audit always required before placing an MCPCB order?
A5: Use risk to set the qualification depth. A document review may suit a low-risk prototype, while restricted, high-volume, safety-relevant, or complex constructions may require deeper site and process evidence. Base the decision on construction complexity, consequence of failure, supply continuity, required origin, and the records available from the named factory.
Q6: What should be frozen after the prototype is approved?
A6: Freeze the released data and the variables that affect equivalence. These normally include the factory, material grade, cross-section, critical drawing notes, test scope, approved deviations, and change-notification rules. Also identify temporary prototype tooling or substitutions so they are not silently carried into the production baseline.
Q7: How should I handle an unusually low quotation?
A7: Run an equal-scope comparison before negotiating price. Check materials, thicknesses, tolerances, tests, tooling, assembly exclusions, quantities, delivery terms, and build site. Ask the supplier to confirm every exception in writing; the remaining difference is then a commercial choice rather than an unidentified technical reduction.
Q8: Can an MCPCB supplier use separate fabrication and assembly factories?
A8: Yes, if ownership and change control are explicit. The quote should name each site and assign responsibility for materials, solder profiles, handling damage, inspection, failures, and corrective action. Confirm who approves fabrication changes and who leads containment when a defect could have originated at either site.
Q9: What evidence should be retained for repeat orders?
A9: Retain the approved revision and lot-linked release records. Material identity, deviations, critical inspection, electrical or isolation results, shipment identity, and approved changes support later comparison and containment. Keep the supplier’s production-site and substitution approvals with the same order identity so a repeat build can be checked against the actual baseline.
Q10: When is a one-stop PCB and assembly supplier useful?
A10: It is useful when fabrication and assembly decisions share the same thermal or mechanical interface. Confirm that one owner coordinates the stackup, soldering process, component risks, heat-sink interface, inspection, and test scope. The quotation should also name the factory and responsible owner for every required process.
This website uses cookies to enhance your experience, remember your preferences, and help us understand how visitors use our site. You can accept all cookies, reject non-essential cookies, or manage your settings.
This website uses cookies to improve your experience while you navigate through the website. Out of these cookies, the cookies that are categorized as necessary are stored on your browser as they are essential for the working of basic functionalities of the website. We also use third-party cookies that help us analyze and understand how you use this website. These cookies will be stored in your browser only with your consent. You also have the option to opt-out of these cookies. But opting out of some of these cookies may have an effect on your browsing experience.
Necessary cookies are absolutely essential for the website to function properly. These cookies ensure basic functionalities and security features of the website, anonymously.
Cookie
Duration
Description
cookielawinfo-checkbox-analytics
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytics".
cookielawinfo-checkbox-functional
11 months
The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional".
cookielawinfo-checkbox-necessary
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Necessary".
cookielawinfo-checkbox-others
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Other.
cookielawinfo-checkbox-performance
11 months
This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance".
viewed_cookie_policy
11 months
The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data.
Functional cookies help to perform certain functionalities like sharing the content of the website on social media platforms, collect feedbacks, and other third-party features.
Performance cookies are used to understand and analyze the key performance indexes of the website which helps in delivering a better user experience for the visitors.
Analytical cookies are used to understand how visitors interact with the website. These cookies help provide information on metrics the number of visitors, bounce rate, traffic source, etc.
Advertisement cookies are used to provide visitors with relevant ads and marketing campaigns. These cookies track visitors across websites and collect information to provide customized ads.