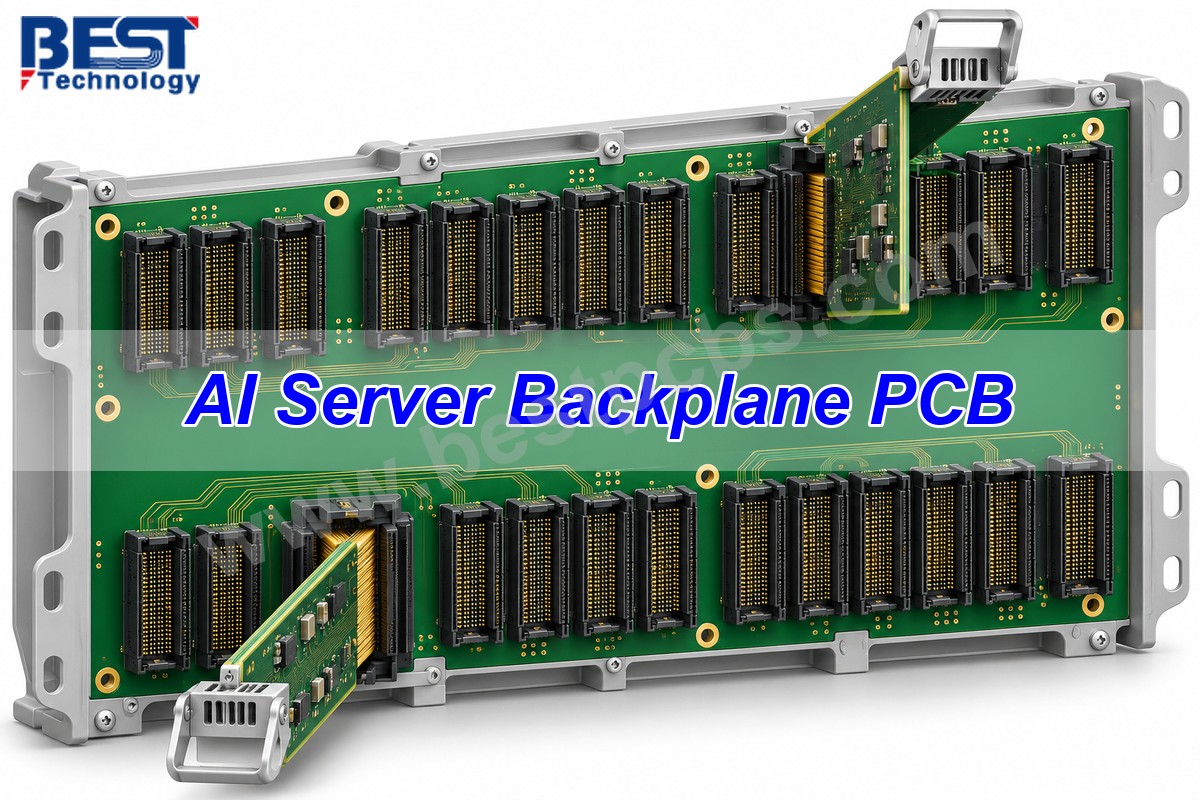
An AI Server Backplane PCB connects computing modules, GPU expansion hardware, storage devices, and power interfaces inside AI servers and high-performance computing systems. These boards often require complex multilayer stackups, low-loss materials, controlled-impedance routing, and high-density connectors to carry fast signals across the system. Their design must also account for power distribution, mechanical stability, and manufacturing tolerances.
At EBest Circuit (Best Technology), we manufacture multilayer PCBs and provide component sourcing, assembly, and testing services. For a custom backplane, we can review the board construction and assembly requirements together, from laminate selection and plated holes to connector placement and the finished deliverable.
Key Takeaways
- An AI server backplane PCB connects computing modules, storage devices, expansion cards, and power interfaces through a common interconnection board.
- Passive backplanes primarily carry signals and power, while active backplanes add components such as PCIe switches, retimers, or management controllers.
- Low-loss PCB laminates help reduce signal attenuation across long, high-speed transmission paths.
- Common impedance targets include 50 Ω single-ended and 85 Ω or 100 Ω differential, depending on the interface specification.
- Backdrilling removes unused via-barrel copper to reduce signal reflections while preserving the copper needed for electrical connections.
- Press-fit connectors require tightly controlled finished-hole diameters, copper plating, and mechanical alignment.
- Electrical testing, TDR impedance measurement, microsection analysis, and high-frequency channel testing help verify backplane manufacturing quality.
What Is an AI Server Backplane PCB?
An AI server backplane PCB is a central interconnection board that links multiple electronic modules through PCB traces, connectors, and power-distribution structures. It allows hardware modules to communicate and receive power without requiring separate point-to-point wiring for every connection.
Its function depends on the server architecture. Common applications include:
- AI and GPU servers
- NVMe storage systems
- Modular compute systems
- Blade server chassis
- Network switching systems
- Server power distribution systems
A backplane may carry PCIe, Ethernet, storage, management, and power connections. Each interface has different electrical requirements.
For example, a PCIe storage backplane connects multiple SSDs through high-speed differential links. Its PCB layout must account for connector transitions, trace loss, and the required PCIe generation.
In some AI server architectures, GPU-to-GPU communication uses dedicated switch boards, module substrates, or cable assemblies. The backplane’s exact role therefore depends on the system’s interconnect architecture.
AI Server Backplane vs Motherboard: What Is the Difference?
An AI server motherboard hosts processors, memory interfaces, controllers, and other primary electronic components. A backplane mainly connects separate computing, storage, or expansion modules. Both may use complex multilayer PCB structures, but their layout priorities differ.
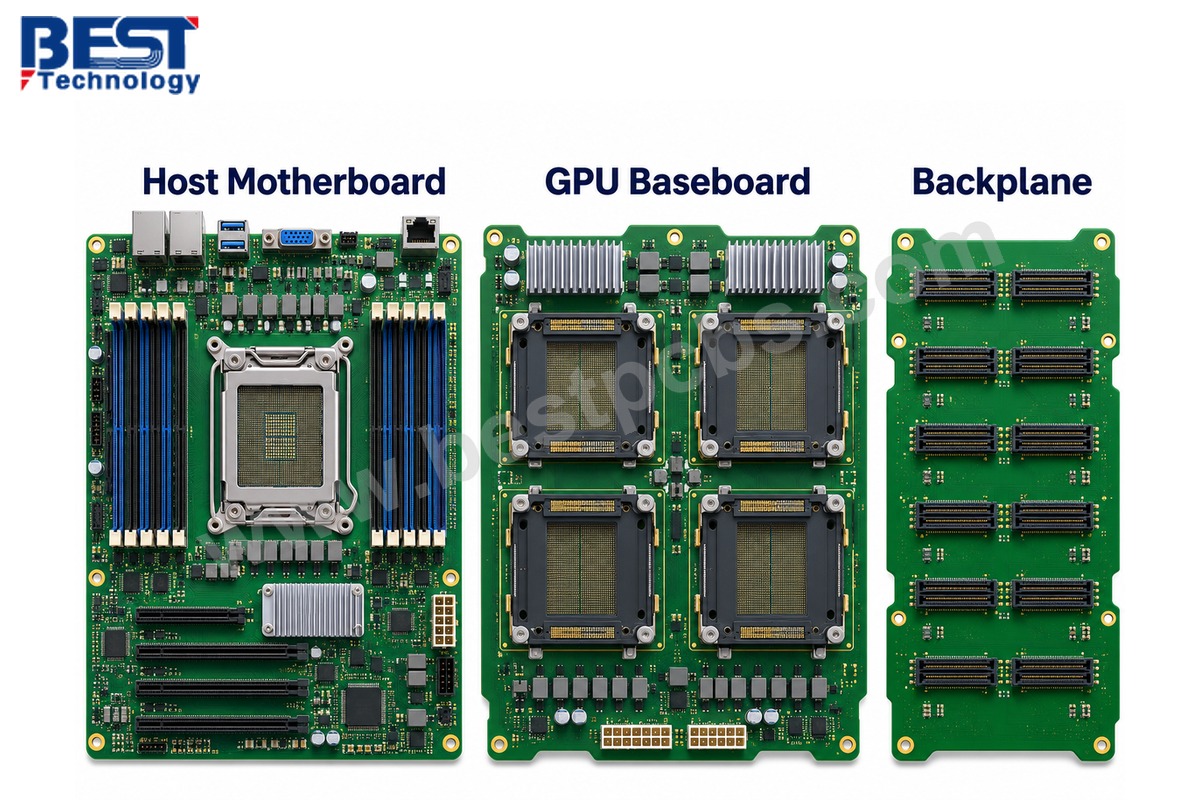
| Feature | AI Server Backplane | AI Server Motherboard |
|---|---|---|
| Main function | Connects hardware modules | Hosts computing components |
| Main features | Connectors and interconnects | CPUs, memory, controllers |
| Routing priority | Module-to-module signals | Chip-to-chip signals |
| PCB construction | Often thick and multilayer | Dense multilayer |
| Key challenge | Signal loss and alignment | BGA routing and power integrity |
| Assembly | Press-fit and SMT | Primarily SMT |
A motherboard typically requires dense BGA breakout routing, fine-pitch component placement, and local power distribution.
A backplane often has longer transmission paths, larger connector arrays, and tighter requirements for mechanical alignment.
Passive vs Active Backplanes: Which Does Your Server Need?
A passive backplane provides electrical connections between modules without actively switching or regenerating signals. An active backplane adds electronic components that perform functions such as signal retiming, switching, monitoring, or management.
Passive Backplane
Passive backplanes are suitable when direct signal connections can meet the system’s electrical requirements.
Typical characteristics include:
- PCB traces and connectors carry signals between modules.
- Power and ground planes provide electrical distribution.
- Fewer active components simplify cooling and maintenance.
- Lower component count can reduce assembly complexity.
A passive backplane may still include passive components such as resistors or capacitors.
Active Backplane
Active backplanes contain ICs that support additional system functions, such as:
- PCIe switches for connecting multiple devices.
- Retimers or redrivers for signal conditioning.
- Storage-management controllers.
- Power monitoring and system-status circuitry.
For example, when a high-speed connection exceeds its allowable channel-loss budget, a retimer may help restore signal quality.
However, retimers require additional PCB space, power, thermal management, and component integration.
Which should you choose? Use a passive backplane when direct connections satisfy the required channel specifications. Choose an active design when signal conditioning, switching, or system-management functions are necessary.
PCB Backplane vs Cable Backplane: Which Should You Choose?
A PCB backplane uses copper traces in a rigid multilayer board, while a cable backplane routes selected signals through cable assemblies. PCB backplanes offer compact connections and integrated power distribution. Cable assemblies can be advantageous for long, high-speed connections where PCB trace loss becomes significant.
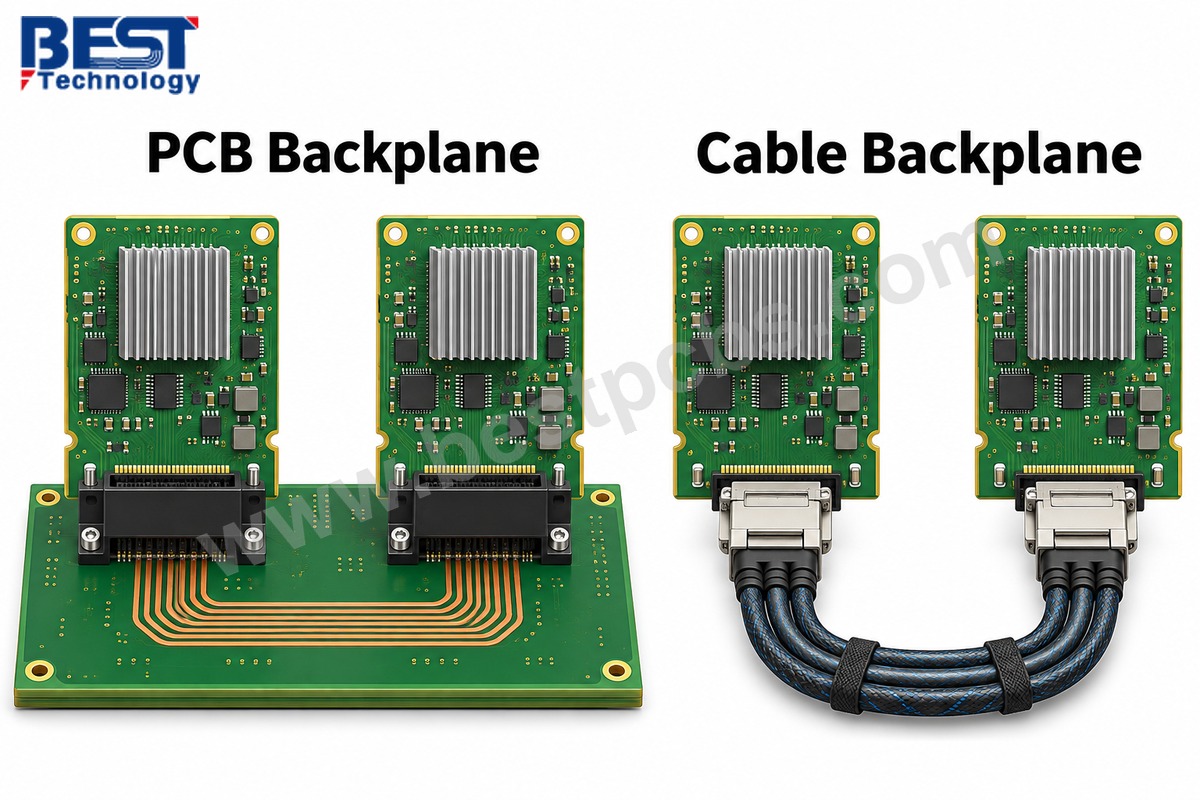
| Factor | PCB Backplane | Cable Backplane |
|---|---|---|
| Signal path | PCB copper traces | Cable conductors |
| Main advantage | Compact integration | Lower loss on some long links |
| Mechanical structure | Rigid board | Flexible routing |
| Power distribution | Integrated planes | Often separate power paths |
| Installation | Board and connectors | Cable assembly and routing |
| Typical use | Dense modular systems | Long high-speed connections |
Some AI servers use both approaches. A rigid PCB handles power and management connections, while high-speed cables carry selected data links.
The decision should be based on complete channel simulations that include connector and transmission-medium losses.
Which Materials Are Used for AI Server Backplane PCBs?
AI server backplanes commonly use high-Tg FR-4, low-loss, or ultra-low-loss PCB laminates. Material selection depends on signal frequency, transmission length, electrical loss, thermal requirements, and the number of PCB layers.
The most important electrical material properties are dielectric constant (Dk) and dissipation factor (Df).
- Dk: Influences signal propagation and the dimensions needed for controlled impedance.
- Df: Indicates dielectric loss at a specified frequency. Lower values generally reduce dielectric attenuation.
- Tg: Characterizes the glass-transition behavior of the laminate.
- CTE: Affects dimensional stability and plated-hole reliability during thermal cycling.
Common Backplane PCB Materials
| Laminate | Typical Dk at 10 GHz | Typical Df at 10 GHz | Tg |
|---|---|---|---|
| FR408HR | 3.65 | 0.0095 | 190°C |
| I-SPEED | 3.63 | 0.0060 | 180°C |
| I-TERA MT40 | 3.45 | 0.0031 | 215°C |
| TACHYON 100G | 3.02 | 0.0021 | 215°C |
High-speed laminate families include Panasonic MEGTRON and Isola Tachyon products. Each family contains different grades, so electrical and thermal properties should be checked against the specific manufacturer’s datasheet.
Copper Foil Selection
Copper surface roughness also affects high-frequency signal loss. As frequency increases, current concentrates closer to the conductor surface, making roughness more relevant to attenuation.
Low-profile or very-low-profile copper foil may be selected for critical high-speed layers.
Hybrid Material Construction
A hybrid stackup uses different dielectric materials within one PCB. For example, low-loss laminates may be placed around critical signal layers, while other layers use materials selected for power distribution or cost control.
Before approving a hybrid structure, the PCB manufacturer should evaluate:
- Material compatibility during lamination.
- Resin flow and bonding requirements.
- Differences in thermal expansion.
- Copper thickness and dielectric spacing.
- Finished board thickness and dimensional stability.
For complex multilayer backplanes, material selection should be completed together with the stackup design rather than treated as a purchasing substitution.
How Are Backplane PCB Layer Count and Thickness Chosen?
Backplane PCB layer count is determined by routing density, connector pin assignments, reference-plane requirements, and power distribution. Finished thickness depends on the stackup, connector specifications, mechanical rigidity, and plated-hole manufacturing limits.
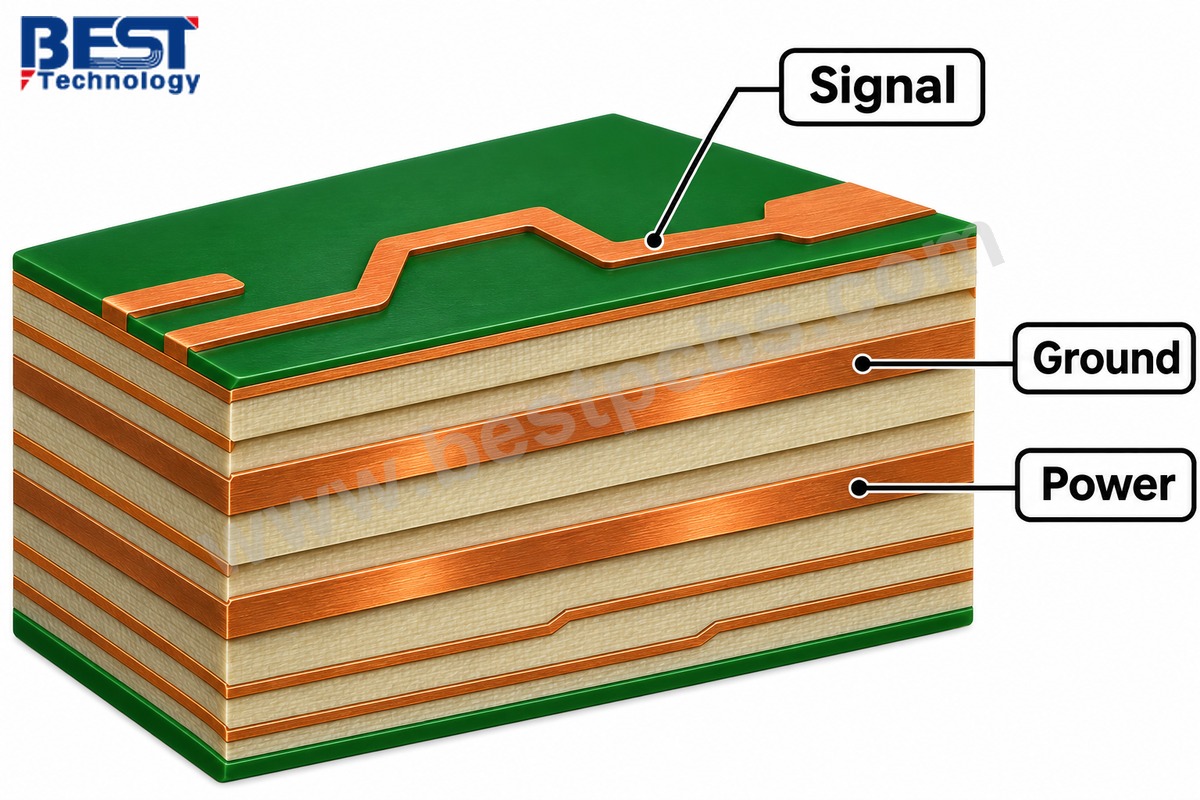
There is no standard layer count for every AI server backplane.
How Is Layer Count Determined?
A complex server backplane may require separate layers for:
- High-speed differential routing.
- Ground reference planes.
- Power distribution.
- Low-speed management signals.
- Connector breakout and routing transitions.
For example, a 24-layer design may use several signal layers separated by ground planes. Power planes and management connections occupy additional layers according to the routing requirements.
Adding layers increases routing capacity, but also affects fabrication cost, lamination complexity, and inspection requirements.
How Is Board Thickness Determined?
Thickness becomes important when large press-fit connector arrays are used.
A thicker PCB can improve mechanical rigidity, but it also creates longer through-hole barrels. Those longer barrels may introduce additional via-stub effects.
The following factors should be checked before approving the thickness:
- Connector-approved PCB thickness.
- Press-fit pin engagement requirements.
- Plated through-hole aspect ratio.
- Available drilling and plating capability.
- Finished board flatness.
- Mechanical support during connector insertion.
The PCB stackup and connector specification should be reviewed together before production drawings are finalized.
What Affects Signal Integrity Across a Backplane?
Signal integrity in an AI server backplane depends on the combined electrical behavior of PCB traces, vias, connectors, reference planes, and dielectric materials. These structures introduce attenuation, reflections, and electromagnetic coupling that must remain within the interface’s channel budget.
The most important factors are controlled impedance, insertion loss, return loss, crosstalk, and differential-pair skew.
1. Controlled Impedance
Controlled impedance keeps transmission-line characteristics within a specified range.
Common nominal targets include:
- 50 Ω for many single-ended lines.
- 85 Ω for certain PCIe differential designs.
- 100 Ω for many other differential interfaces.
Actual targets depend on the interface specification.
Impedance is affected by trace width, spacing, copper thickness, dielectric height, and material Dk.
For example, a 100 Ω differential pair with a manufacturing tolerance of ±10% has an acceptance range of 90–110 Ω.
2. Insertion Loss
Insertion loss describes signal attenuation through the channel, usually expressed in decibels at specific frequencies.
Major contributors include:
- Long copper traces.
- Dielectric loss.
- Copper surface roughness.
- Connector transitions.
- Via discontinuities.
For long server-backplane channels, selecting a low-loss laminate and optimizing trace geometry can reduce attenuation.
3. Return Loss
Return loss describes signal reflections caused by impedance discontinuities.
Common causes include abrupt trace transitions, connector launches, via geometry, and unused via stubs.
Reducing discontinuities improves impedance consistency and helps preserve signal quality.
4. Crosstalk
Crosstalk occurs when energy from one signal path couples into a nearby signal path.
It can be reduced through appropriate differential-pair spacing, reference planes, routing arrangements, and connector pin assignments.
5. Differential-Pair Skew
Differential-pair skew occurs when the two conductors have different propagation delays.
Length mismatch, dielectric variation, and routing geometry can contribute to skew.
High-speed designs should follow interface-specific skew limits instead of applying one universal length-matching rule.
The complete signal path should be evaluated through channel simulation and, where necessary, S-parameter measurements.
When Does a Backplane PCB Need Backdrilling?
1. Backdrilling Removes Unused Copper from Plated Through-Holes.
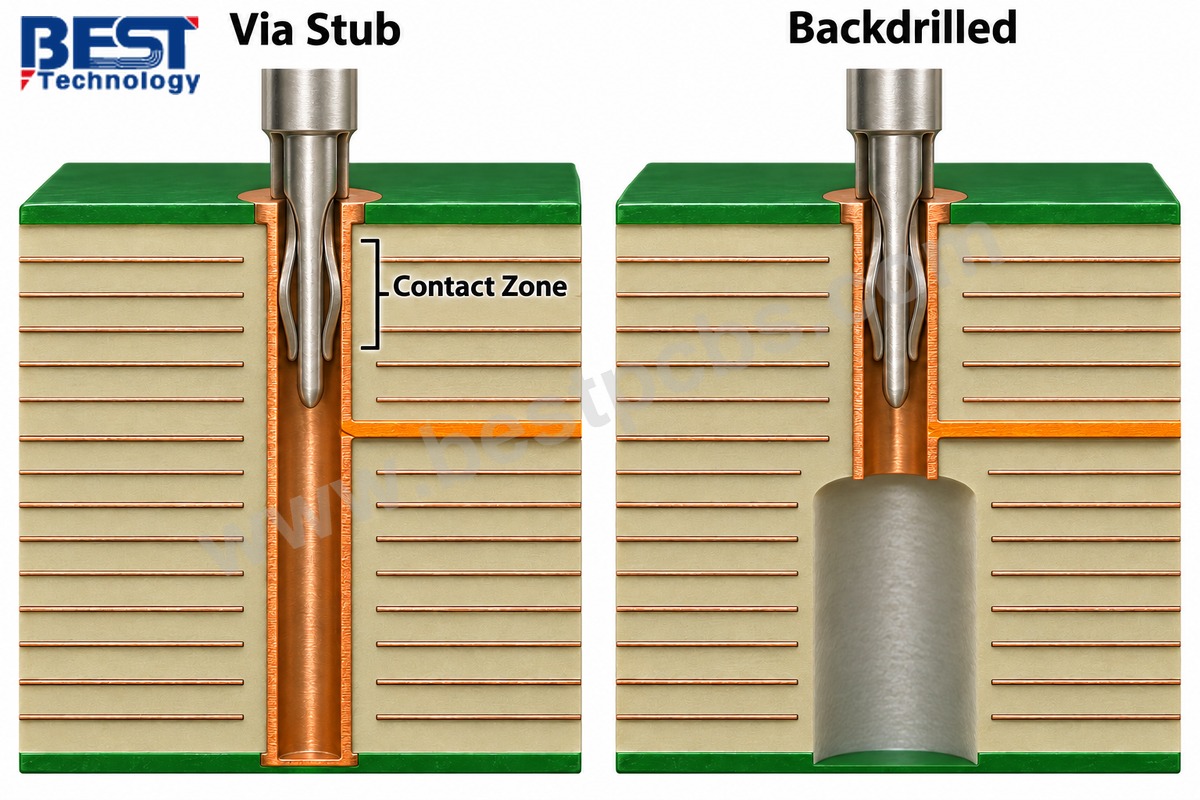
When a signal travels through only part of a via, the remaining unused copper barrel can cause signal reflections and affect high-speed signal transmission. Backdrilling removes this excess copper to improve signal integrity. The term “stub” refers to a via stub, not an electrical short circuit.
2. Backdrilling Depth Must Be Carefully Controlled.
If the drilling depth is too shallow, excess copper may remain. If the drill goes too deep, it may damage the electrical connections that need to be preserved. PCB fabrication drawings should clearly specify the drilling side, target drilling depth, and maximum allowable residual stub length.
3. Press-Fit Connector Holes Require Special Attention During Backdrilling.
Press-fit connector pins rely on the plated copper barrel for electrical contact and mechanical retention. If backdrilling removes copper from the pin’s contact area, it may compromise the electrical connection and long-term reliability of the connector.
What Do Backplane Connectors Require from the PCB?
Backplane connectors require accurate finished-hole dimensions, reliable copper plating, and precise mechanical alignment. High-density press-fit connectors place particular demands on PCB drilling, plating, board thickness, and flatness.
A press-fit connector uses compliant pins that deform during insertion into plated through-holes. The resulting contact pressure provides electrical connectivity and mechanical retention without a conventional solder joint.
Key Press-Fit Connector Requirements
| Parameter | Requirement |
|---|---|
| Finished hole diameter | Connector-specific tolerance |
| Hole copper plating | Approved thickness and quality |
| Hole position | Accurate pin-array alignment |
| PCB thickness | Within connector specification |
| Board flatness | Suitable for connector seating |
| Backdrilling | Preserve the contact region |
Finished-Hole Diameter
Hole diameter is one of the most important manufacturing controls.
An undersized hole can increase insertion force and damage the plated barrel. An oversized hole can reduce contact pressure and mechanical retention.
Finished-hole tolerance must follow the connector manufacturer’s application specification.
Copper Plating Quality
Press-fit pins establish contact with the plated barrel, so plating thickness and hole-wall quality are critical.
Microsection inspection can verify copper thickness, plating continuity, and internal-layer connections.
Connector Alignment and Board Support
Large connector arrays may generate significant insertion forces.
The PCB should include appropriate support locations, mounting features, and clearance for insertion tooling. Connector position and board flatness should also be checked during dimensional inspection.
For high-speed connectors, the recommended footprint, ground-via arrangement, and signal-launch geometry should be followed to maintain channel performance.
How Does a Backplane Distribute Power?
A power-carrying backplane distributes current through connector contacts, copper planes or traces, and vias. Resistance anywhere along that path causes voltage drop and heating, so the narrowest copper section is not the only potential bottleneck.
The relationships are:
ΔV = I × R
P = I² × R
Here, ΔV is voltage drop in volts, I is current in amperes, R is the resistance of the path being evaluated in ohms, and P is the power dissipated in watts.
For an illustrative 20 A path with 2 mΩ resistance, the voltage drop is 0.04 V and the dissipated power is 0.8 W. At 40 A through the same resistance, the drop becomes 0.08 V and dissipation rises to 3.2 W. Doubling current therefore produces 4 times the heating in that path.
Wider copper, additional copper layers, and suitable via arrays can reduce board resistance. Connector contact ratings and temperature rise remain part of the same design. Current sharing between parallel contacts also depends on the connector construction and routing, so multiplying a single-contact rating by the contact count can overstate capacity.
Some servers use separate power distribution boards or busbars. Their full system current should not be assigned to a signal backplane that carries only local auxiliary power.
How Are AI Server Backplane PCBs Tested?
AI server backplane PCBs are tested through electrical inspection, impedance measurement, structural analysis, and dimensional verification. High-speed designs may also require channel measurements to confirm insertion loss and return loss.
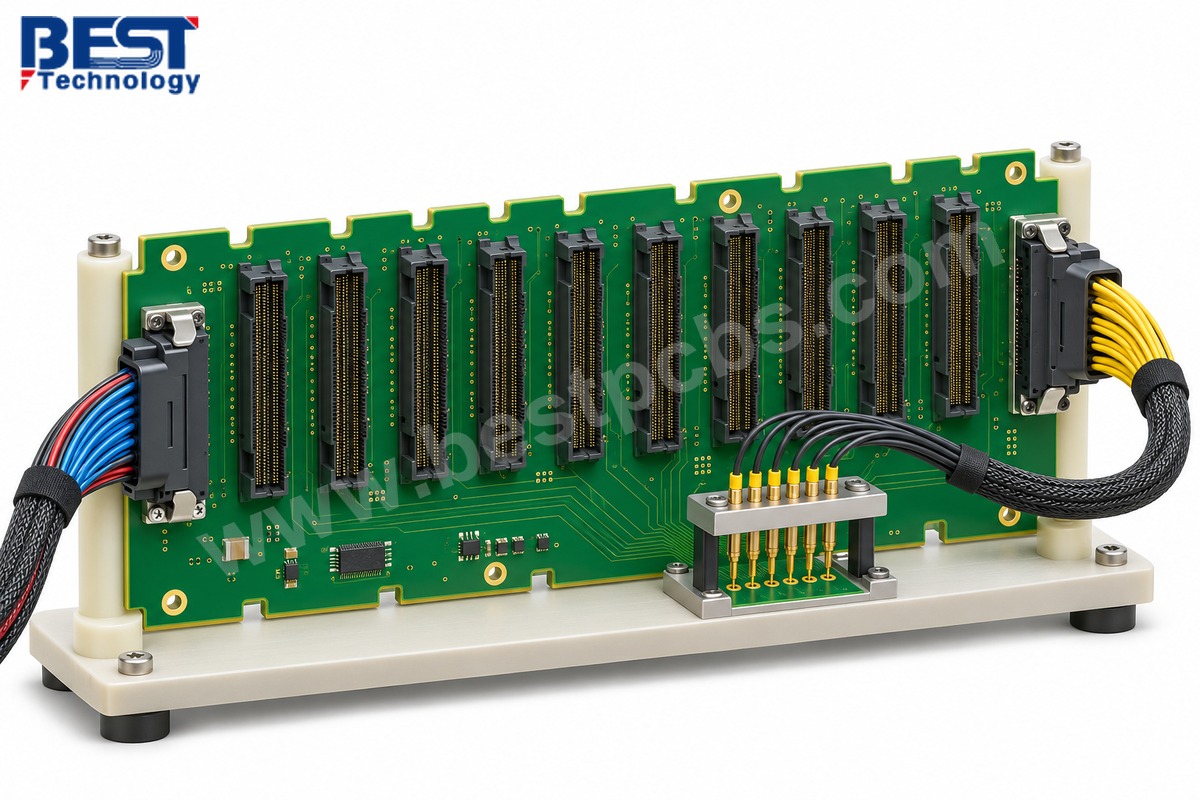
Each test addresses a different manufacturing or electrical requirement.
| Test Method | Main Verification |
|---|---|
| Electrical test | Opens and shorts |
| TDR | Controlled impedance |
| Microsection | Plating and layer structure |
| AOI | Copper pattern defects |
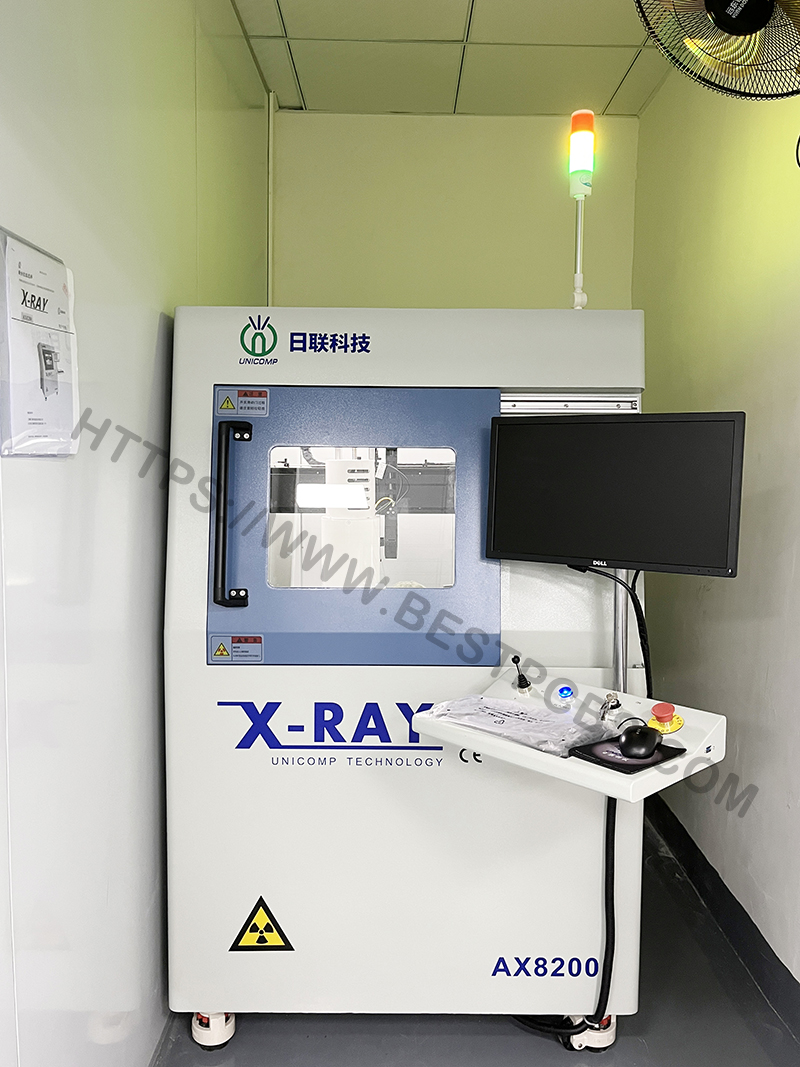
| X-ray | Selected internal features |
| Dimensional inspection | Holes, thickness, alignment |
| VNA | High-frequency channel behavior |
Electrical Testing
Electrical continuity and isolation testing verifies that the intended connections are present and unintended connections are absent.
This is particularly important for large backplanes containing dense connector arrays and numerous signal nets.
TDR Impedance Testing
Time-domain reflectometry measures transmission-line impedance.
For example, a 100 Ω differential impedance specification with ±10% tolerance gives an acceptance range of 90–110 Ω.
Measurements are commonly performed on representative impedance coupons according to the approved test method.
Microsection Inspection
Microsection inspection provides a cross-sectional view of the PCB structure.
It can verify:
- Plated through-hole copper thickness.
- Inner-layer interconnection quality.
- Layer alignment.
- Dielectric spacing.
- Backdrilling depth and residual stubs.
AOI and X-Ray Inspection
AOI identifies copper-pattern defects such as opens, shorts, and spacing deviations during fabrication.
X-ray inspection helps examine selected internal structures that optical equipment cannot directly inspect.
High-Frequency Channel Testing
Critical high-speed channels may require vector network analyzer measurements.
S-parameter measurements can characterize insertion loss, return loss, and other transmission properties. The results should be compared with the approved channel specifications.
Why Choose EBest Circuit for Your Backplane PCB Project?
EBest Circuit combines complex multilayer PCB manufacturing, high-speed engineering support, and coordinated assembly services to help customers develop reliable server hardware. Our engineering review identifies manufacturing concerns before fabrication, helping customers reduce avoidable revisions and production delays.
1. Experience with Complex AI Server PCBs
Our FR-4 PCB capabilities cover standard builds from 1–10 layers and special-process builds up to 32 layers. For 1 oz copper, our listed standard inner- and outer-layer trace/space capability is 4/4 mil, approximately 0.10/0.10 mm, with 3/3 mil available through special processing. Designs with 8 layers or more use high-Tg material under our fabrication requirements.
Our engineers review:
- Multilayer stackup structures.
- Low-loss material requirements.
- Controlled-impedance routing.
- Drilling and backdrilling specifications.
- Connector hole tolerances.
- Board thickness and mechanical requirements.
This allows fabrication requirements to be assessed against the customer’s actual PCB design.
2. Engineering Review to Reduce Manufacturing Risks
Our engineering review helps identify issues before production begins.
For backplane projects, the review can examine:
- Stackup feasibility and material availability.
- Via structures and plated-hole aspect ratios.
- Backdrilling depth and residual stub limits.
- Press-fit connector hole specifications.
- Impedance requirements and test coupons.
- Manufacturing tolerances and inspection access.
Customers receive engineering feedback that can help prevent unnecessary PCB revisions, connector-fit issues, and production delays.
3. PCB Fabrication and Assembly Under One Coordinated Service
EBest Circuit provides PCB manufacturing, component sourcing, SMT assembly, through-hole assembly, and testing support.
Our assembly equipment includes Yamaha YSM20R placement equipment, 3D SPI, nitrogen reflow, wave soldering, AOI, and X-ray inspection.
For active backplanes, this allows PCB fabrication and component assembly requirements to be reviewed together.
4. Flexible Ordering and Engineering Communication
EBest Circuit supports engineering prototypes, low-volume projects, and repeat manufacturing .
For complex backplanes, actual fabrication capabilities and lead times are confirmed after reviewing the layer count, material, board thickness, drilling structure, and testing requirements.
Send your Gerber or ODB++ files, stackup, connector specifications, target impedance, quantities, and testing requirements to sales@bestpcbs.com. Our engineers can provide an engineering review and project-specific quotation.
FAQ
What Is the Difference Between a Midplane and a Backplane?
A midplane usually connects modules mounted on opposite sides of a central board, while a backplane commonly provides connections behind a group of modules. Product naming varies, so the mechanical arrangement and connection diagram determine the actual layout.
Can the Same Backplane Support SATA, SAS and NVMe Drives?
Yes, some backplanes support multiple drive interfaces, but the connectors, lane routing, and controller must support each intended protocol. A board designed only for SATA or SAS does not gain NVMe support because a drive fits the bay.
Are U.2, U.3 and EDSFF Backplanes Interchangeable?
No, they are not generally interchangeable. U.2 and U.3 compatibility depends on the drive, backplane, and controller implementation, while EDSFF uses different defined form factors and connector arrangements. The platform’s supported-drive list is the practical reference for a replacement.
Does Every AI Server Backplane Support Hot Swapping?
No. Hot swapping requires suitable connectors, power-control behavior, and support from the controller, firmware, and operating system. A removable drive or module is not automatically safe to insert or remove while powered.
Does an AI Server Backplane Always Need HDI?
No. Through-hole multilayer construction can suit backplanes whose connector routing and signal requirements allow it. HDI becomes useful when dense connector fields or fine-pitch active components need interconnections that conventional through vias cannot accommodate efficiently.
Can a Higher-Speed Backplane Upgrade an Older Server?
Not by itself. The host, endpoints, connectors, cables, and firmware must all support the intended interface generation. A newer backplane cannot raise the link rate above the capabilities of the connected devices.
Conclusion
An AI Server Backplane PCB must combine reliable high-speed signal transmission, controlled multilayer construction, accurate connector interfaces, and stable power distribution. Material loss, impedance, via stubs, PCB thickness, and press-fit hole quality all influence the finished board’s performance.
EBest Circuit supports complex AI server PCB projects with multilayer fabrication, engineering review, controlled-impedance manufacturing, and coordinated assembly services. Send your design files and technical requirements to sales@bestpcbs.com for an engineering review and quotation.