ADAS ECU hardware must process camera, radar, and vehicle-network data without allowing dense routing, power noise, hidden solder joints, or uncontrolled revisions to weaken the main board. For buyers, the practical challenge is not simply finding a factory that can produce a multilayer PCB. It is making sure the PCB structure, component package plan, assembly process, inspection method, and production files work together.
EBest Circuit (Best Technology) supports PCB fabrication, component sourcing, PCBA, inspection, and customer-defined testing for complex automotive electronics. Send your stackup requirements, Gerber files, BOM, placement data, and test instructions to sales@bestpcbs.com for a manufacturability review of your ADAS computing board.
How Is an ADAS ECU Different from Its PCB and PCBA?
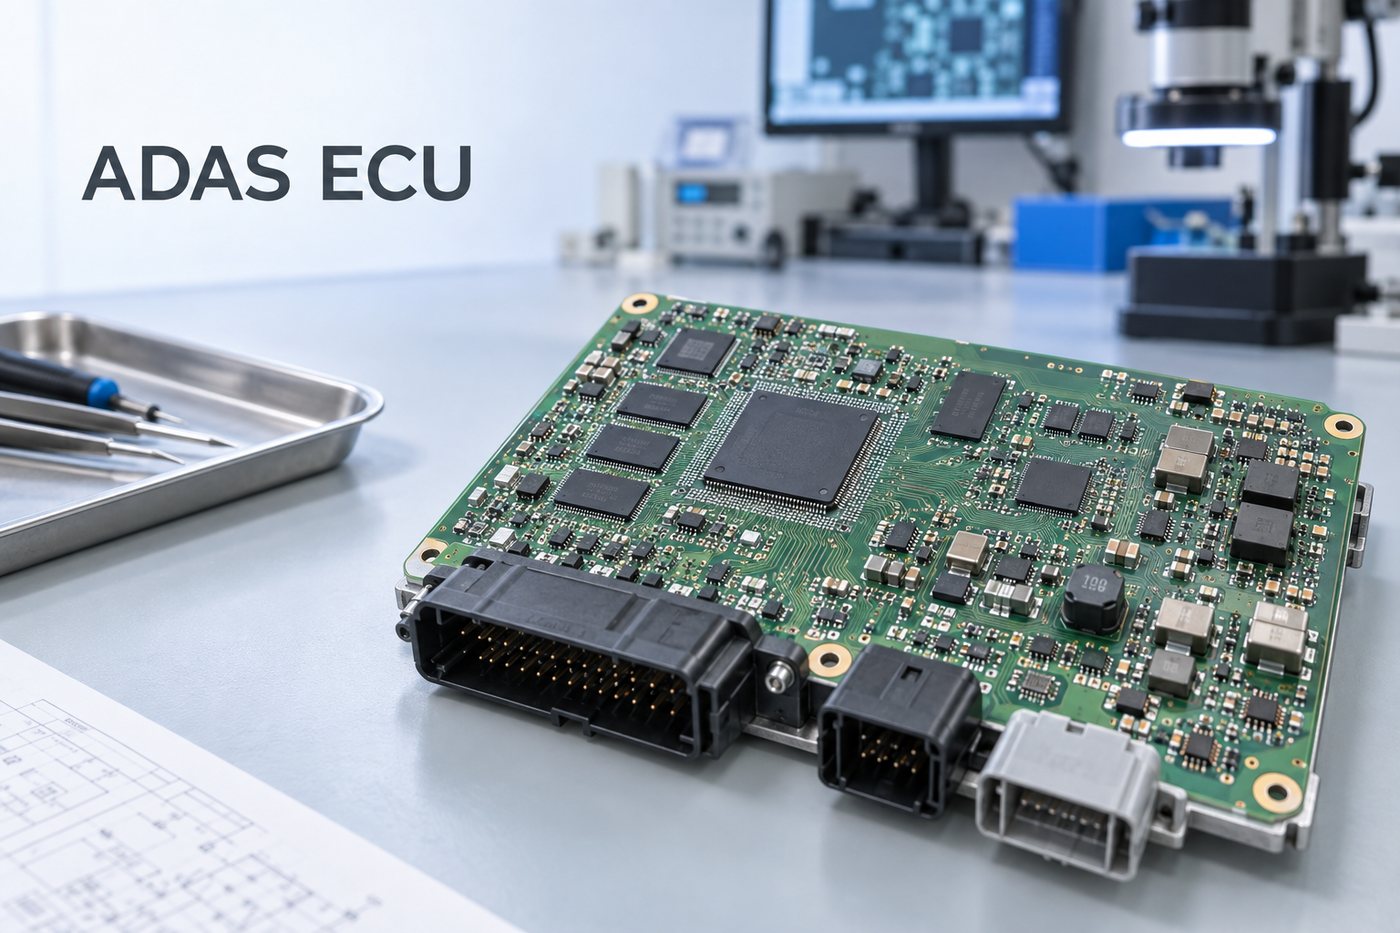
An ADAS ECU is the complete electronic control unit used to support advanced driver-assistance functions. Unlike a general electronic control unit board, it is specifically built around the sensing, computing, and communication demands of driver-assistance functions. Depending on the vehicle architecture, it may receive data from cameras, radar sensors, ultrasonic sensors, inertial sensors, or other vehicle controllers. It then runs perception, decision, or sensor-fusion software and exchanges commands or status information with other vehicle systems.
The PCB and PCBA are only parts of that complete controller:
- ADAS ECU: The complete unit, which may include the PCBA, firmware, application software, connectors, enclosure, shielding, thermal materials, and mechanical mounting.
- ADAS ECU PCB: The bare printed circuit board before components are assembled.
- ADAS ECU PCBA or main board: The populated board containing the processor, memory, power circuits, communication interfaces, and supporting components.
This distinction defines the manufacturing responsibility. A PCB and PCBA supplier can review the board for fabrication and assembly, build the bare board, source specified parts, assemble the components, inspect solder joints, and perform agreed tests. Sensor-fusion algorithms, vehicle calibration, functional-safety concepts, cybersecurity, and final vehicle validation normally remain with the customer and its system-development partners.
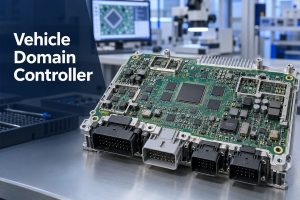
An ADAS domain controller is a more centralized form of automotive controller. It may consolidate work previously divided among several function-specific ECUs and process more sensor channels on one computing platform. That consolidation can increase processor pin count, memory bandwidth, interface density, power demand, and PCB routing pressure, but it does not change the boundary between the complete controller and the PCBA inside it.
What Components Are Assembled on an ADAS ECU Main Board?
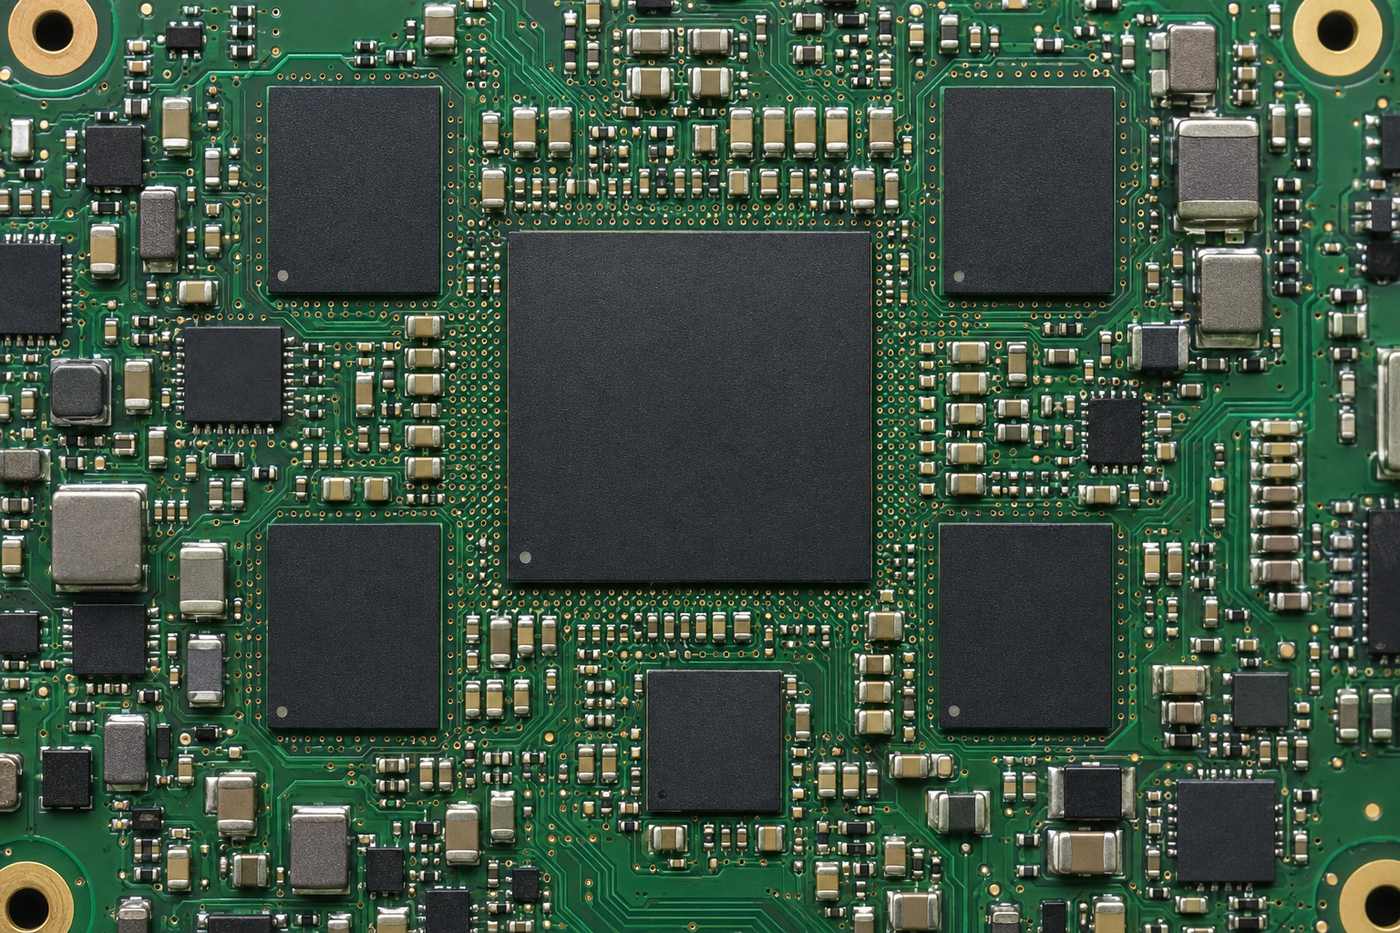
The ADAS ECU architecture on the main board is usually built around a high-performance processor or system-on-chip. The precise component set depends on the number and type of sensor inputs, the software workload, and the vehicle network architecture. A typical board may include:
- A main SoC, processor, MCU, GPU, or dedicated acceleration device
- LPDDR4 or LPDDR5 memory close to the processor
- eMMC, UFS, NOR flash, or other nonvolatile storage
- PMICs, DC-DC converters, load switches, supervisors, and protection devices
- MIPI CSI-2, serializer/deserializer, PCIe, Ethernet, CAN or CAN FD, SDIO, SPI, and I2C interfaces
- Oscillators, clock buffers, filters, ESD protection, and common-mode components
- Board-to-board, automotive data, power, and service connectors
These parts do not create equal manufacturing difficulty. A large BGA processor and nearby LPDDR devices control fanout and layer planning. Camera and high-speed network channels create impedance and return-path requirements. PMICs and processor rails require low-inductance power delivery. Connectors and protection devices influence component clearance, mechanical support, and EMC behavior.
For the buyer, the useful question is therefore not “How many components are on the board?” It is “Which packages, interfaces, and power rails control the PCB structure and assembly process?” Identifying those controlling features early prevents an apparently complete layout from reaching fabrication with an impractical via structure, incomplete impedance definition, or insufficient inspection access.
When Does an ADAS ECU PCB Require HDI or Additional Layers?
An ADAS ECU PCB does not automatically require HDI. HDI becomes justified when conventional through-hole fanout and the available layer count cannot route the required signals while maintaining reference planes, power distribution, spacing, and manufacturable feature sizes.
The decision is usually driven by five conditions:
- BGA pitch and escape density. Fine-pitch processor or memory packages may leave too little room for conventional vias between pads.
- Number of high-speed channels. Multiple camera, memory, PCIe, or Ethernet channels need controlled routing space and continuous reference planes.
- Board outline and connector locations. A restricted enclosure or fixed connector arrangement can compress routing into a small area.
- Power and ground requirements. A high-current processor with several voltage rails may need additional plane area, local copper, and dedicated return paths.
- EMC and isolation constraints. Sensitive high-speed circuits, switching power sections, and external interfaces may need physical separation that consumes routing area.
A higher layer count can provide more routing channels and better separation between signal and power structures, but more layers alone do not solve a poor breakout. HDI circuit boards may use laser microvias, blind vias, buried vias, or via-in-pad around fine-pitch BGAs. Each option affects cost, registration tolerance, plating, lamination cycles, inspection, and repairability.
The most economical structure is the least complex stackup that still routes the board with acceptable impedance, return paths, copper distribution, and manufacturing margins. Before release, the PCB manufacturer should review BGA pitch, finished board thickness, via aspect ratio, annular ring, microvia depth, copper weight, material selection, and the proposed lamination sequence.
How Do LPDDR4, MIPI CSI-2, and eMMC Affect the PCB Stackup?
ADAS sensor fusion can place heavy and simultaneous demands on camera inputs, working memory, and stored data. LPDDR4, MIPI CSI-2, and eMMC serve different functions on the board, but they share one basic requirement: the stackup must provide predictable routing layers and uninterrupted reference paths before detailed routing is finalized.
LPDDR4 connects the processor to working memory through a wide, timing-sensitive bus. Memory placement, breakout geometry, reference-plane continuity, via count, and routing length must be planned as one system. Manufacturing cannot correct a topology or timing problem after the Gerber files are released, but the fabricator can verify that the selected trace widths, spacings, dielectric thicknesses, and via structures can be produced consistently.
MIPI CSI-2 commonly carries camera data into the processing platform, sometimes through serializer/deserializer devices rather than a direct camera-to-processor connection. Differential-pair impedance, intra-pair geometry, transitions, stubs, and the return path through connector regions all matter. A nominal impedance value is not sufficient if the fabrication drawing does not identify the controlled structures and their tolerances.
eMMC combines storage, command, and clock connections in a compact package. Although its routing burden may be smaller than a wide LPDDR interface, package breakout, clock quality, power integrity, and proximity to the processor can still affect placement and layer use. SDIO and other synchronous interfaces create similar concerns when clock rate and routing length increase.
The customer should release an impedance table together with the stackup and identify the nets that use each structure. The manufacturer can then calculate manufacturable trace geometries using the selected laminate and copper thickness, return the proposed stackup for approval, and use impedance coupons or agreed test methods to confirm the finished board.
How Should BGA Fanout and Vias Be Planned Around the Processor and Memory?
BGA fanout should be planned from the package pitch inward, not selected after routing becomes congested. The first review should compare pad diameter, solder-mask strategy, escape-channel width, finished hole size, annular ring, and the number of I/O rows that must reach internal layers.
For a package that allows through-hole escape, conventional vias may provide the lowest-cost and most repairable solution. As pitch decreases or the number of inner rows increases, through-holes can occupy too much routing area. Laser microvias or via-in-pad structures can open additional escape channels, but they add process controls. Filled and capped via-in-pad features must meet flatness and plating requirements so that solder does not drain into the via or leave an uneven BGA land.
Memory placement also affects fanout. Short processor-to-LPDDR connections may compete with power decoupling, eMMC routing, and processor power escapes. Moving the memory slightly can sometimes remove an HDI bottleneck; in other designs, the enclosure, thermal solution, or timing budget prevents that change. This is why the package drawing, placement, stackup, and routing constraints should be reviewed together.
Fabrication data should clearly identify blind-via spans, buried-via spans, filled vias, capped vias, back drilling if used, and any special acceptance criteria. Ambiguous via notes can cause quotation errors or, more seriously, a board built with a structure different from the designer’s intent.
How Is an ADAS ECU PCBA Assembled and Inspected?
Automotive PCBA assembly for an ADAS ECU requires controls that match the actual package mix. The main processor, memory, storage, PMICs, small passives, bottom-terminated components, and large automotive connectors do not necessarily share the same solder-paste or thermal needs.
Stencil apertures and paste volume should be reviewed in high-density BGA and QFN areas as well as around thermally demanding power components. Component moisture sensitivity, bake requirements, feeder setup, placement accuracy, and the reflow profile must be controlled for the specified parts and board thermal mass. Large copper areas or thick multilayer constructions can change heating behavior across the assembly.
Inspection methods must also match what can be seen:
- SPI checks solder-paste deposits before components hide the pads.
- AOI checks visible placement, polarity, component presence, and accessible solder joints.
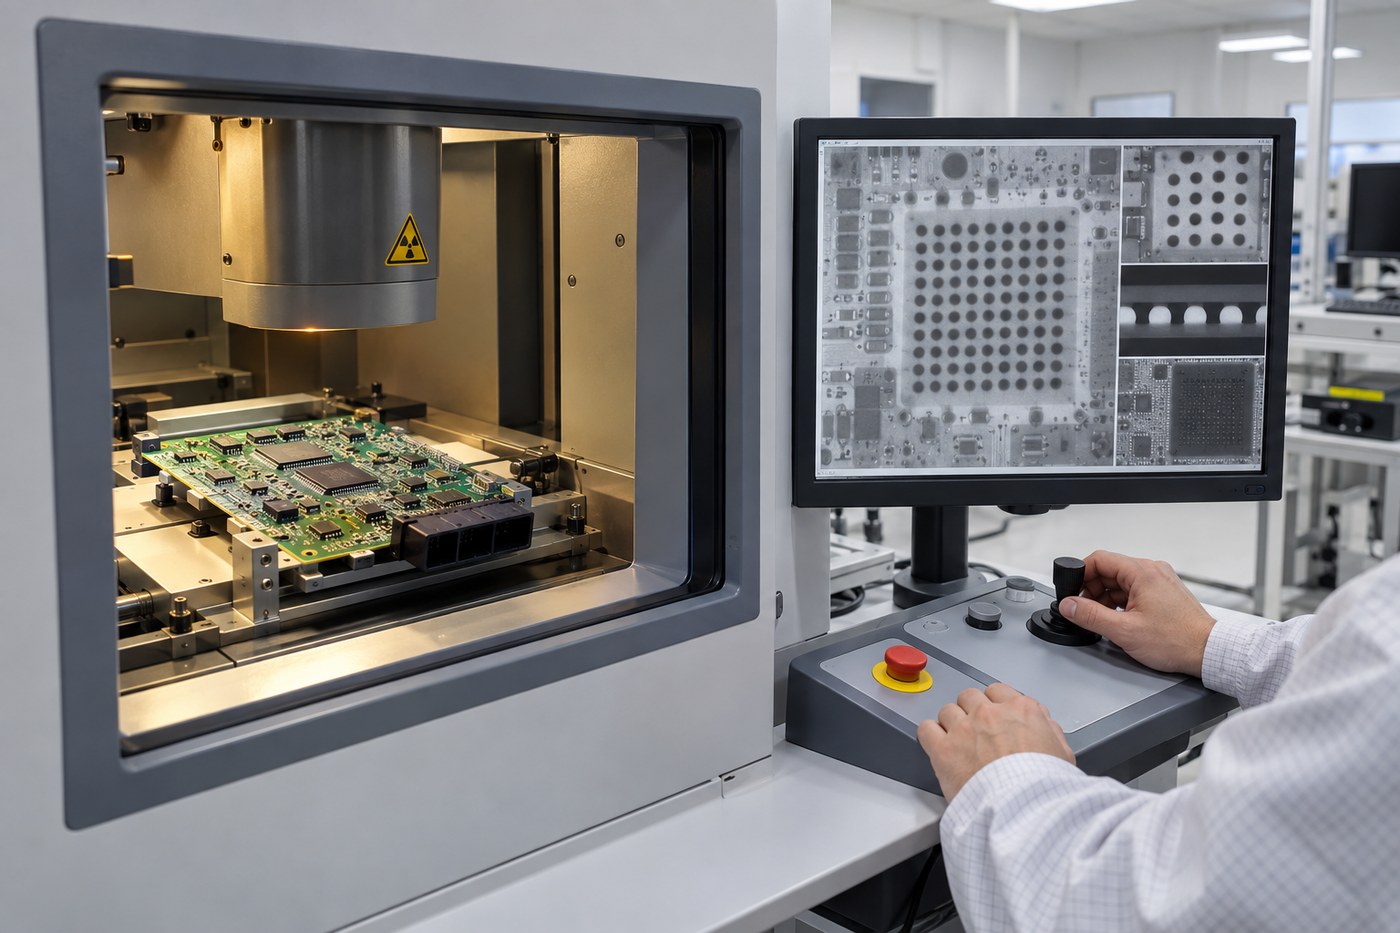
- X-ray inspection evaluates hidden BGA, QFN, and via-in-pad solder regions for defects such as excessive voiding, bridging, opens, or abnormal solder distribution.
- Electrical and functional tests verify the circuits and functions defined by the customer’s test coverage, fixtures, firmware, and acceptance limits.
X-ray is important, but it is not a substitute for process control or electrical testing. A visually acceptable BGA image cannot prove that every high-speed channel, memory connection, or power rail functions correctly. Buyers should therefore define which boards are X-rayed, which joints or regions are reviewed, how results are recorded, and what functional test is required after assembly.
EBest Circuit can coordinate PCB fabrication, specified component sourcing, assembly, AOI, X-ray, and agreed electrical or functional testing. The customer should supply approved firmware, test procedures, fixtures or fixture requirements, and acceptance criteria whenever programming or functional verification is included.
How Can an ADAS ECU Prototype Be Prepared for Repeatable PCBA Production?
A working prototype is not automatically ready for repeatable production. Repeatability starts when the approved design, materials, process assumptions, and acceptance evidence are converted into a controlled manufacturing package.
Before the next build, the customer and manufacturer should close the following items:
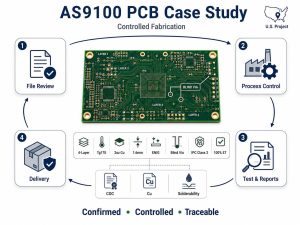
- Freeze matching revisions of the Gerber or ODB++ data, fabrication drawing, assembly drawing, BOM, centroid file, and approved change records.
- Confirm the stackup, laminate, copper weight, impedance structures, HDI build, surface finish, and any special via filling or capping.
- Resolve BOM lifecycle, lead-time, package, polarity, and approved-alternative questions before purchasing.
- Record stencil decisions, reflow conditions, BGA or QFN X-ray criteria, and any workmanship requirements that differ from the normal process.
- Define programming files, software versions, fixture ownership, test steps, pass/fail limits, and required test records.
- Preserve traceability between the board revision, BOM revision, assembly lot, component lots, and test results when the project requires it.
This preparation protects the buyer from three common production problems: building the wrong revision, accepting an unapproved component substitution, and discovering too late that the prototype test depended on an undocumented setup. It also makes quotation and scheduling more accurate because the factory can see which materials, special processes, inspections, and tests belong to the released configuration.
For a new supplier transfer, do not rely only on the previous purchase order. Provide the current controlled package and identify any deviation accepted on earlier builds. A short pre-production review can expose conflicts among the PCB drawing, BOM, placement file, assembly notes, and test instructions before material is committed.
FAQs About ADAS ECU
Is an ADAS domain controller the same as an ADAS ECU?
Not always. An ADAS ECU may perform one defined driver-assistance function, while an ADAS domain controller usually consolidates several functions or sensor channels on a more centralized computing platform. Both contain PCBAs, but a domain controller often creates higher processing, memory, interface, power, and thermal demands.
Does every ADAS ECU PCB need HDI?
No. HDI is appropriate when BGA pitch, fanout density, board size, interface count, or routing constraints cannot be handled efficiently with through-hole vias and a conventional multilayer stackup. The decision should follow a layout and manufacturability review.
How many layers should an ADAS ECU PCB use?
There is no universal number. The layer count depends on BGA escape needs, high-speed signal groups, reference planes, power rails, EMC separation, copper weight, and the available board area. The stackup should be agreed before routing is finalized.
How are hidden BGA solder joints inspected?
X-ray inspection is used to evaluate solder distribution and identify visible evidence of bridging, opens, excessive voiding, or other abnormalities beneath the package. It should be combined with SPI, AOI, process records, and appropriate electrical or functional tests.
What files are needed to quote an ADAS ECU PCB and PCBA?
Provide the Gerber or ODB++ data, fabrication drawing, stackup and impedance requirements, BOM, assembly drawing, centroid file, and any special workmanship, programming, inspection, or test instructions. Include the expected quantity and revision so the quotation reflects the intended build.
If you need a manufacturing review for an ADAS ECU PCB or high-density PCBA, send the controlled project files and expected build quantity to sales@bestpcbs.com. EBest Circuit (Best Technology) can review the fabrication, sourcing, assembly, inspection, and agreed testing scope before production.