





PCBA process control manages the materials, equipment settings, soldering conditions, and production checks that determine PCB assembly quality. It combines defined operating limits with measurements and a clear response when the process changes. The aim is consistent production across boards, shifts, and repeat orders, with issues addressed during manufacturing rather than discovered only at final inspection.
At EBest Circuit, our four SMT lines are supported by solder paste inspection (SPI), automated optical inspection (AOI), and X-ray inspection. Our manufacturing execution system (MES) links material usage, process history, and inspection data, giving our team a way to investigate a specific build rather than relying on a final pass/fail report.
What Is PCBA Process Control?
PCBA process control is the ongoing management of the variables that affect assembly results, including material condition, paste deposition, component position, and soldering temperature.
It connects machine settings with what actually happens on the board. Squeegee pressure is a printer setting; the solder paste volume deposited on a pad is a measurable result. Both belong in the control system, because an approved machine recipe still needs verification on the assembly.
Product inspection and process control therefore serve different purposes. Inspection decides whether an assembly meets its acceptance requirements. Process control manages the conditions used to produce it.
Consider a solder bridge found after reflow. Removing the bridge corrects that board. Reviewing the relevant paste deposits, placement alignment, and soldering conditions helps identify the source of the problem. The production change should follow the evidence, with subsequent boards checked to confirm its effect.
What Should a PCBA Process Control Plan Include?
A PCBA process control plan should identify each controlled characteristic, its requirement, the checking method and frequency, the responsible person, and the response to an abnormal result.
The following examples show how those requirements can translate into line-side instructions. They are a starting point, not a completed production plan.
| Operation | Control point | Verification | Initial response to a confirmed issue |
|---|---|---|---|
| Material release | PCB revision and component identity | BOM, drawing, and label checks | Hold the affected kit |
| Paste printing | Deposit volume, height, and offset | SPI against validated limits | Hold affected boards; review printing |
| Placement | Position, orientation, and polarity | First-article checks and applicable AOI | Review program and feeder setup |
| Reflow | Peak temperature and time above liquidus | Measured board profile | Assess affected boards; verify the recipe |
| Electrical testing | Connections and specified functions | Approved test program | Separate product faults from test-system faults |
Each row still needs product-specific limits, sampling or check intervals, ownership, and release authority. Include startup, replenishment, maintenance, and changeover checks where relevant.
Assemblies requiring cleaning or coating also need controls for those operations. The plan should follow the actual manufacturing route.
How Are PCBs and Components Controlled Before Assembly?
PCBs and components are controlled before assembly by confirming that the released materials match the build documents and remain suitable for the intended process.
Three checks cover the main preparation work:
- PCB identity and condition: Confirm the part number, revision, specified finish, packaging condition, and relevant incoming acceptance requirements.
- Component identity: Match the manufacturer part number, package, value, and approved alternatives to the bill of materials (BOM). Resolve substitutions before releasing the kit.
- Handling condition: Check moisture-sensitive packaging and exposure history, while maintaining electrostatic discharge (ESD) protection during storage, kitting, and loading.
For moisture-sensitive devices, floor life is tied to the device’s moisture sensitivity level and handling conditions. Track exposure after opening the moisture-barrier bag and apply the relevant manufacturer and J-STD-033 instructions.
Baking should follow that assessment, with the device and packaging temperature limits considered. Specify PCB drying separately from component baking, using each supplier’s instructions rather than one shared recipe.
Keep accepted and held materials clearly separated at the point of use.
How Is Solder Paste Printing Controlled in PCBA?
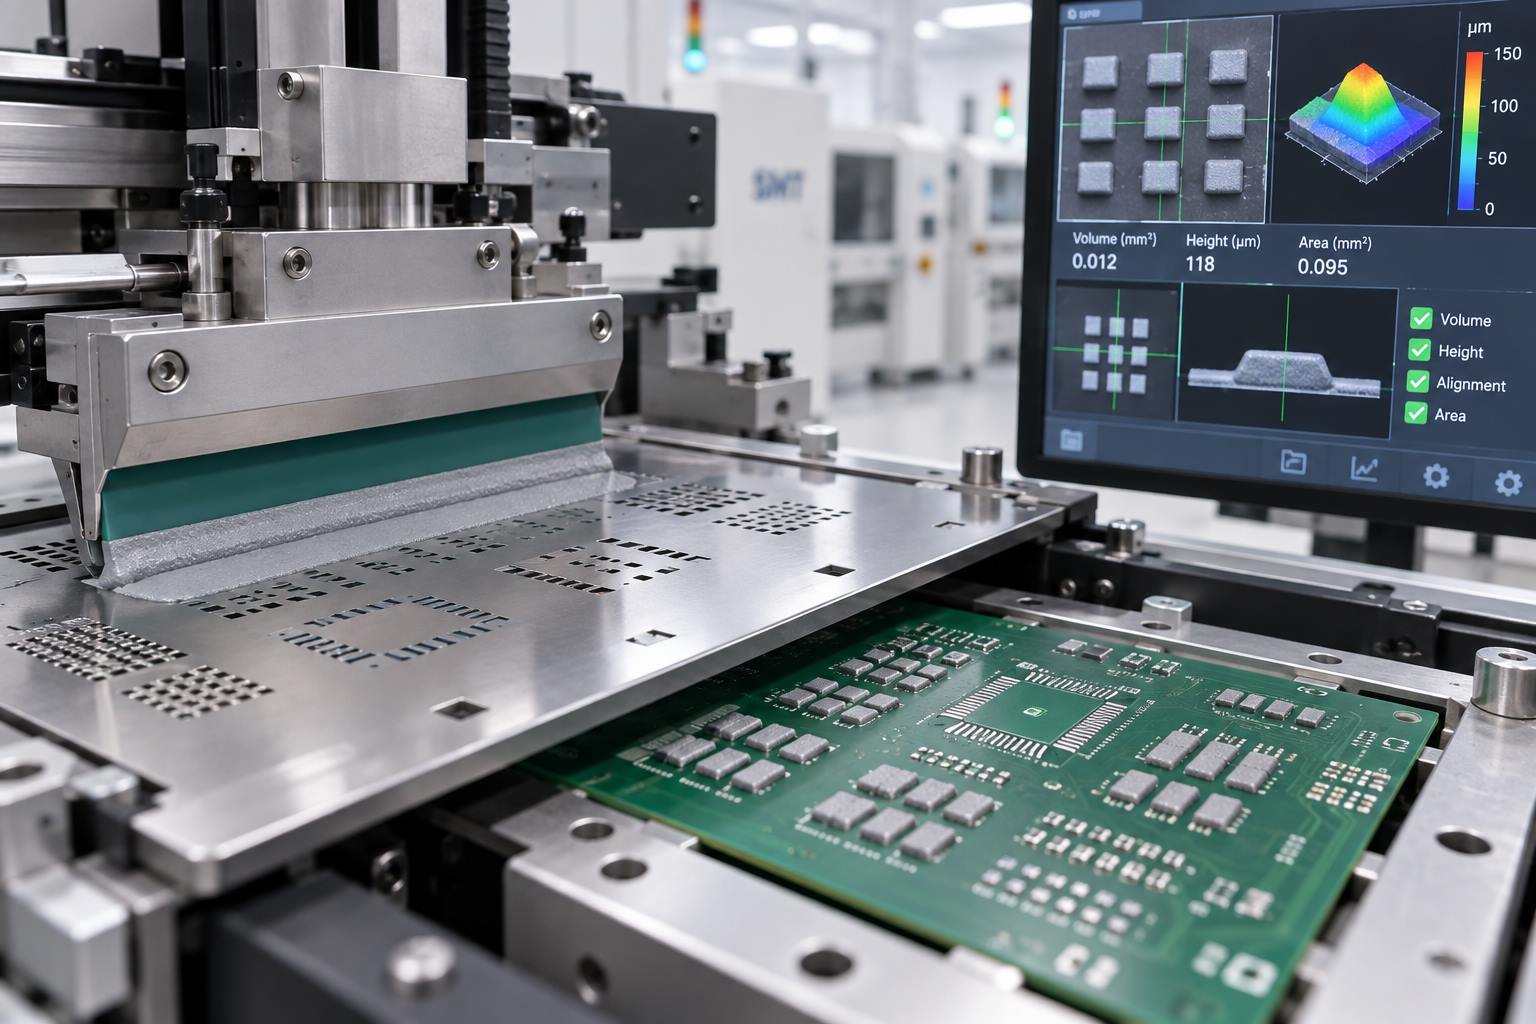
Solder paste printing is controlled by keeping the paste, stencil, printer setup, and board support within a verified operating window.
The main controls work together:
- Paste condition: Use the specified alloy and flux system, following the supplier’s storage, conditioning, and working-life instructions.
- Stencil and support: Confirm the stencil revision, aperture condition, underside cleanliness, and support beneath the printed area.
- Printer settings: Control alignment, squeegee pressure and speed, stencil separation, and the cleaning cycle.
SPI then checks the result on the board, including deposit volume, height, area, and offset. Set the inspection limits for the relevant pad geometry and assembly requirements.
A useful investigation starts with the pattern. As an example, repeated low deposits around one fine-pitch package justify checking those apertures and local board support. A shift across the entire panel calls for an alignment review.
Verify the next prints after an adjustment. For a confirmed failed print, keep the board out of placement until it has an approved disposition, including any required cleaning and reprinting.
How Is Component Placement Accuracy Controlled in PCBA?
Component placement accuracy is controlled through correct placement data, verified feeder loading, maintained pickup hardware, and checks on the populated board.
The setup has three distinct parts:
- Program: Coordinates, board side, rotation, package definition, fiducial recognition, and placement height.
- Material loading: Correct reel or tray, feeder assignment, component orientation, and replenishment checks.
- Pickup hardware: Suitable nozzles, clean pickup surfaces, reliable vacuum, and correctly indexed feeders.
A first-article check confirms that the setup matches the assembly drawing, especially around polarized devices and fine-pitch packages. Repeat the affected checks after a relevant program, material, or setup change.
Keep positional accuracy separate from component identity. A part can be accurately placed while still being the wrong value or manufacturer part number. Feeder verification addresses that distinction.
During production, review pickup errors and repeated offsets by feeder, nozzle, and component location. In a troubleshooting example, errors associated with one feeder should prompt a local investigation before changing the coordinate origin for the entire board.
How Is the Reflow Soldering Profile Controlled in PCBA?
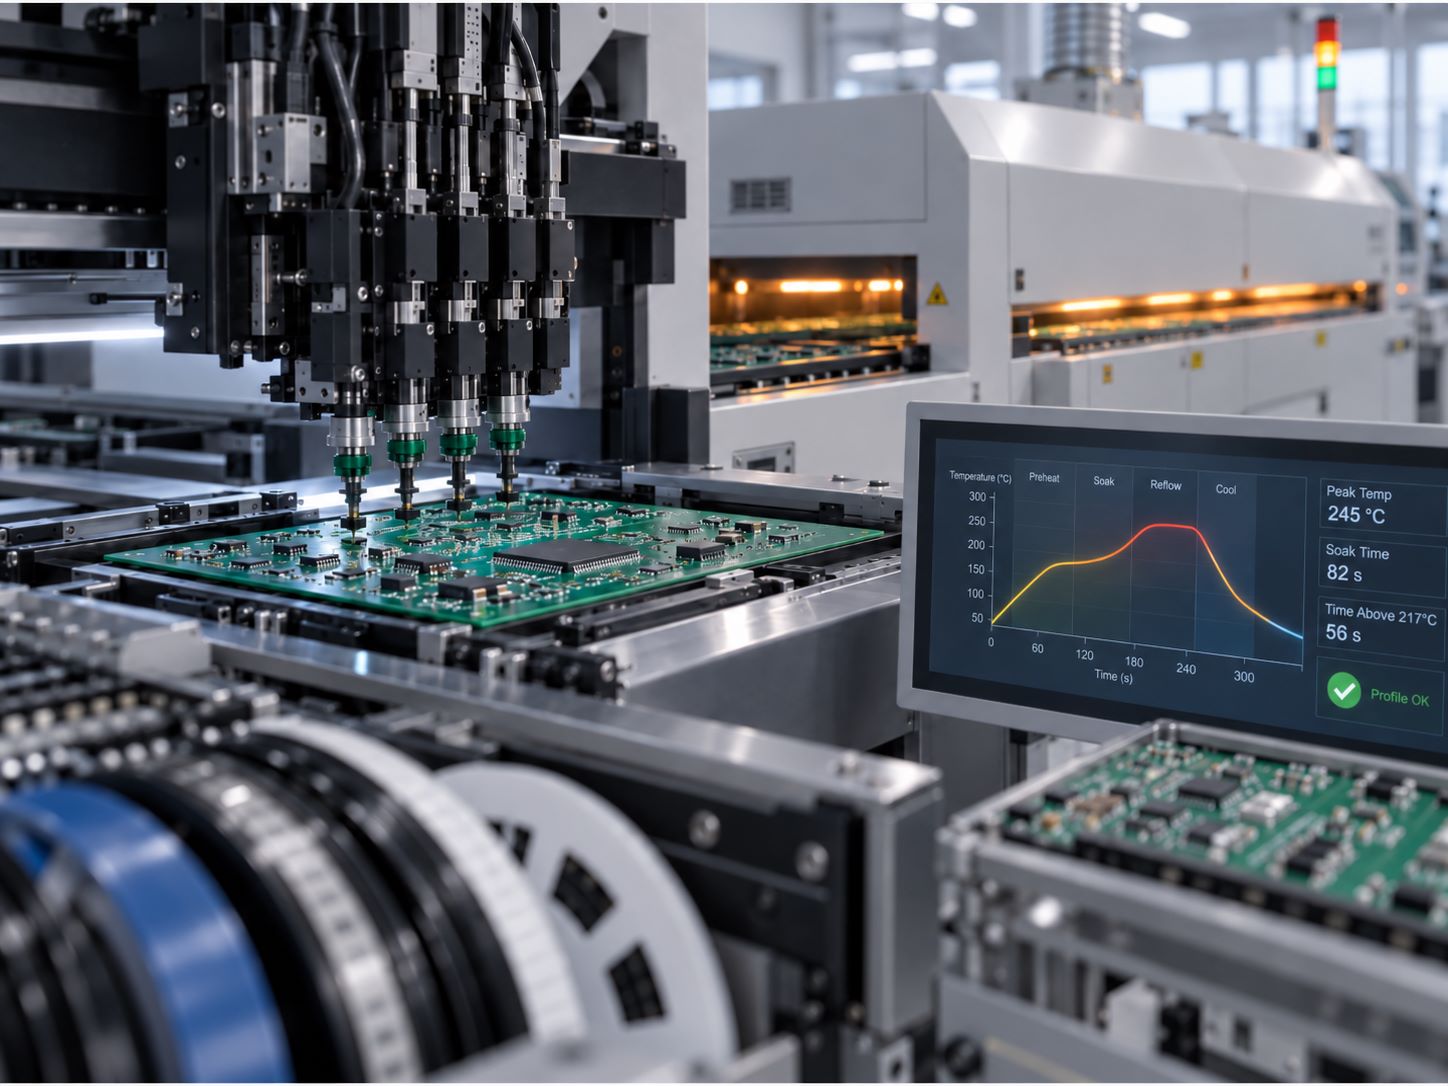
The reflow soldering profile is controlled by measuring temperature over time on a representative assembly and comparing the measurements with the approved thermal window.
That window must accommodate the solder paste, components, and PCB. The main measurements are:
| Profile measurement | What it establishes |
|---|---|
| Heating rate | How quickly the assembly heats |
| Soak, when specified | Exposure through the selected pre-reflow temperature range |
| Peak temperature | Highest temperature at each monitored location |
| Time above liquidus | Duration above the solder alloy’s liquidus temperature |
| Cooling rate | How quickly the assembly cools after reflow |
These measurements should be evaluated together against the selected solder paste’s process requirements.
Attach thermocouples at relevant solder-joint and component locations, including areas expected to heat fastest and slowest. A dense connector area and a small component near the board edge may experience different profiles.
Use the measured results to establish oven zone settings and conveyor speed. Component temperature ratings constrain the profile, while the solder paste has its own process requirements.
Oven setpoints are not the same as temperatures measured on the assembly. Retain the qualified profile with the recipe so repeat builds have a defined thermal reference.
How Is Through-Hole Soldering Controlled in PCBA?
Through-hole soldering is controlled through flux application, board preheat, solder temperature, contact conditions, and inspection of the completed joints.
The settings depend on the soldering method:
| Method | Main controls |
|---|---|
| Wave soldering | Flux coverage, preheat, solder temperature, wave height, conveyor speed, and contact time |
| Selective soldering | Flux location, preheat, nozzle condition, solder temperature, travel path, and dwell time |
| Hand soldering | Tip size and condition, verified temperature, solder and flux selection, and contact time |
These controls address how flux and heat reach the joint, rather than relying on the solder-pot or iron temperature alone.
Preheat prepares the flux and raises the assembly temperature before solder contact. Areas connected to substantial copper deserve particular attention during thermal verification.
For an insufficient-hole-fill investigation, review heat delivery and flux coverage alongside lead-to-hole fit and solder access. Increasing solder temperature alone may leave the underlying issue unresolved.
Inspect wetting, hole fill, bridging, and other applicable features against the agreed acceptance criteria. Group joints by their demonstrated process needs where appropriate; a large power connector and a small signal header may need different selective-soldering settings.
How Do Inspection and Test Data Support PCBA Process Control?
Inspection and test data support PCBA process control by showing which defects recur, where they occur, and whether an adjustment improves the result.
Organize findings by reference designator, defect type, board identity, and production time. Compare like-for-like builds and consistent test coverage when reviewing trends.
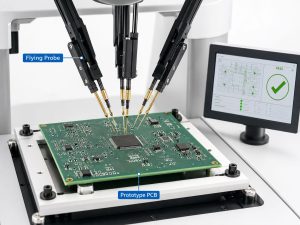
For example, repeated AOI findings at the same component location provide a starting point for checking the placement and soldering process. Confirm the reported condition before changing settings. Electrical failures also warrant a fixture and probe-contact check, since test-system faults can affect results.
Track first-pass yield separately from final yield. First-pass yield counts assemblies that complete the defined operation successfully without repair or retest.
Suppose 100 boards enter a test operation, 96 pass immediately, and four pass after rework. First-pass yield is 96%, while final yield is 100%. Keeping both figures shows the work required to achieve the shipment result.
How Is SPC Used to Monitor PCBA Process Stability?
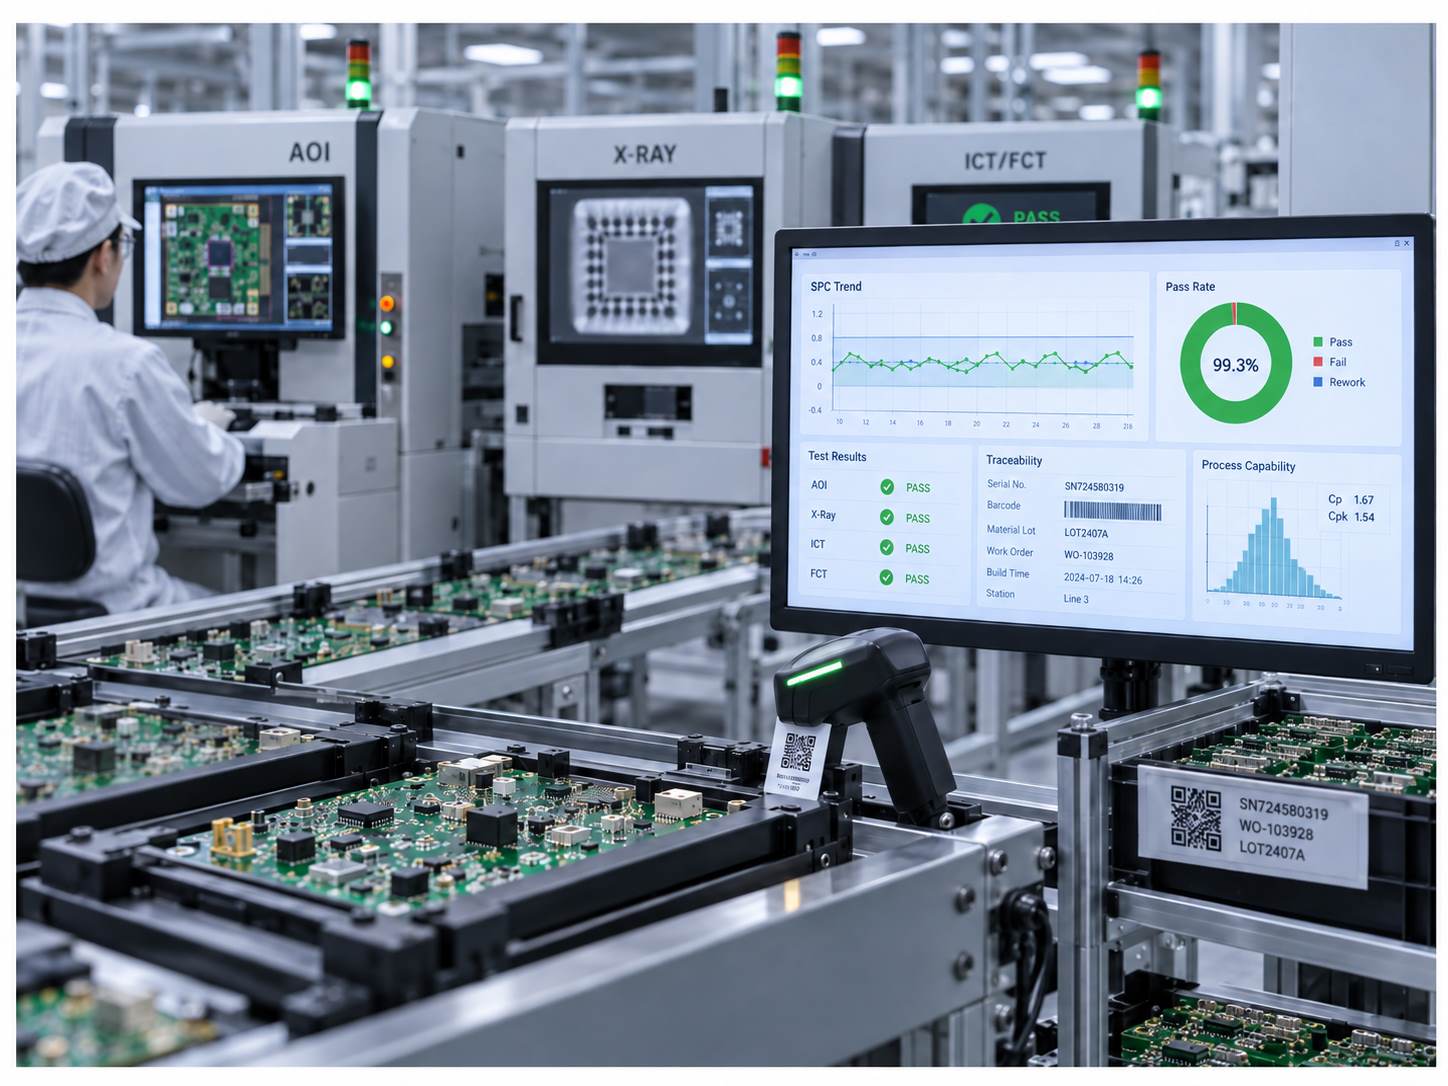
Statistical process control (SPC) monitors PCBA process stability by tracking comparable measurements over time and looking for statistically meaningful changes.
Start with a defined characteristic, such as paste volume for one pad type. Confirm measurement repeatability, collect data in production order, and select a control chart suited to the data and sampling method.
The distinction between limits is important:
- Control limits come from process data and help identify changes in behavior.
- Specification limits come from engineering or customer requirements and define acceptable output.
- Capability indices, including Cp and Cpk, compare a stable process with those specification limits.
For example, a paste-volume trend can trigger investigation while individual deposits remain within specification. Follow the chart’s defined signal rules rather than adjusting the printer after every small fluctuation.
Evaluate capability after confirming stability and suitable data assumptions. Standard Cp and Cpk interpretation assumes normally distributed measurements. Group pads with different volume targets separately so their individual process behavior remains visible.
How Are PCBA Process Deviations Handled?
PCBA process deviations are handled by confirming the issue, containing potentially affected assemblies, correcting the cause, and verifying conditions before production resumes.
A practical response follows five steps:
- Confirm the finding. Check the board, measurement, equipment status, and applicable program. Determine whether the issue is a product defect, process deviation, or measurement error.
- Establish the affected scope. Identify the relevant material lot, production interval, equipment, and boards. Hold potentially affected assemblies while their status is evaluated.
- Investigate the cause. Compare the issue with feeder changes, replenishment, maintenance, material substitutions, and process adjustments. Use measurements and controlled trials to test the likely explanation.
- Correct and verify. Apply the approved action, repeat the relevant setup or first-article checks, and confirm that subsequent results meet the defined requirements.
- Authorize restart and product disposition. Release the process through the designated approver. Separately decide whether held boards can be released, reworked, repaired with authorization, or scrapped.
In a wrong-reel example, the affected scope includes boards populated since that reel was loaded. Replacing the reel fixes the ongoing setup; the already-built boards still require evaluation.
Continue the specified monitoring after restart and update the relevant instruction when the investigation identifies a lasting process change. A successful trial supports restart; the follow-up results show whether the correction remains effective.
What Records Are Needed for PCBA Process Traceability?
PCBA process traceability requires records that connect an assembly’s batch or serial number with its materials, manufacturing history, and quality results.
The record structure should cover:
- Materials: PCB and component lots, solder paste identity, approved substitutions, and relevant exposure records.
- Manufacturing: BOM and drawing revisions, equipment and program versions, production timestamps, and applicable process measurements.
- Quality: Inspection and test results, failure locations, rework, retests, and final release decisions.
Set the traceability detail and retention period before production. IPC-1782 provides a risk-based framework covering manufacturing and supply-chain traceability, with the required scope agreed between customer and supplier.
Record resolution determines how precisely an investigation can identify affected product. Lot-level information supports batch-level tracking; unit-level links can narrow the scope when the underlying material and process records support that detail.
A useful verification exercise works in both directions: select a finished board and retrieve its history, then select a component lot and identify the assemblies that used it. Include reworked boards in the exercise so replacement components remain connected to the final assembly.
FAQs About PCBA Process Control
1. Which IPC Standards Apply to PCBA Process Control?
IPC J-STD-001 covers soldering materials, methods, and process requirements; IPC-A-610 covers assembly acceptance. J-STD-033 supports moisture-sensitive component handling, and IPC-1782 addresses traceability. Agree on the applicable revisions, product class, and customer requirements before the build.
2. How Often Should a PCBA Reflow Profile Be Verified?
Verify it during qualification, at the interval defined in the control plan, and after changes that could affect board temperatures. Relevant triggers include a new thermal recipe, significant oven maintenance, or changes to the assembly’s thermal characteristics.
3. Can SPC Be Used for Low-Volume PCB Assembly?
Yes, when the measurements are comparable and the dataset supports the chosen method. Small batches may need data accumulated across comparable runs. Use setup verification and first-article checks while establishing a baseline, and assess capability only when its statistical prerequisites are met.
4. Does Every PCBA Require X-Ray Inspection?
No. X-ray coverage should reflect hidden-joint risks, package types, and customer requirements. BGA and QFN connections are common candidates. Define the inspected features and acceptance limits as part of the inspection plan.
5. When Do Component Substitutions Require PCBA Process Revalidation?
Revalidation is needed when a substitution changes conditions covered by the approved process, such as package geometry, moisture sensitivity, or temperature limits. Review the change first, then specify the affected placement, soldering, inspection, and test checks.
For a new PCBA build or a repeat order with changes, send your Gerber files, BOM, placement data, assembly drawings, and test requirements to sales@bestpcbs.com. Include the required IPC class and any inspection or traceability deliverables.
EBest Circuit provides PCB fabrication, component sourcing, assembly, and testing. Share critical packages, approved substitutions, and previous manufacturing concerns with the project files so the engineering review can focus on the PCBA process control your assembly needs.
You may also like
Tags: PCBA Process Control, PCBA Process Traceability, PCBA Quality Control